EP0814188B1 - Nappe nontissée formée de filaments continus très fins - Google Patents
Nappe nontissée formée de filaments continus très fins Download PDFInfo
- Publication number
- EP0814188B1 EP0814188B1 EP97108364A EP97108364A EP0814188B1 EP 0814188 B1 EP0814188 B1 EP 0814188B1 EP 97108364 A EP97108364 A EP 97108364A EP 97108364 A EP97108364 A EP 97108364A EP 0814188 B1 EP0814188 B1 EP 0814188B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- filaments
- web
- line
- elementary
- dtex
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 239000004744 fabric Substances 0.000 title description 3
- 239000002131 composite material Substances 0.000 claims description 39
- 238000004519 manufacturing process Methods 0.000 claims description 21
- 229920002292 Nylon 6 Polymers 0.000 claims description 19
- 238000000034 method Methods 0.000 claims description 18
- -1 polyethylene terephthalate Polymers 0.000 claims description 15
- 229920000139 polyethylene terephthalate Polymers 0.000 claims description 15
- 239000005020 polyethylene terephthalate Substances 0.000 claims description 15
- 230000008569 process Effects 0.000 claims description 9
- 238000003490 calendering Methods 0.000 claims description 7
- 238000004043 dyeing Methods 0.000 claims description 7
- 239000000463 material Substances 0.000 claims description 6
- 230000000712 assembly Effects 0.000 claims description 5
- 238000000429 assembly Methods 0.000 claims description 5
- 239000012530 fluid Substances 0.000 claims description 5
- 230000009471 action Effects 0.000 claims description 4
- 238000001816 cooling Methods 0.000 claims description 4
- 230000015572 biosynthetic process Effects 0.000 claims description 2
- 238000004049 embossing Methods 0.000 claims description 2
- 239000002184 metal Substances 0.000 claims description 2
- 238000009736 wetting Methods 0.000 claims 1
- 238000000926 separation method Methods 0.000 description 18
- 239000000835 fiber Substances 0.000 description 11
- 239000011248 coating agent Substances 0.000 description 9
- 238000000576 coating method Methods 0.000 description 9
- 239000004753 textile Substances 0.000 description 9
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 8
- 238000009826 distribution Methods 0.000 description 7
- 229920000642 polymer Polymers 0.000 description 7
- 238000009987 spinning Methods 0.000 description 7
- 239000002861 polymer material Substances 0.000 description 6
- 229920001410 Microfiber Polymers 0.000 description 5
- 238000007596 consolidation process Methods 0.000 description 5
- 239000004745 nonwoven fabric Substances 0.000 description 5
- 239000000126 substance Substances 0.000 description 4
- 239000004698 Polyethylene Substances 0.000 description 3
- 238000005299 abrasion Methods 0.000 description 3
- 239000010410 layer Substances 0.000 description 3
- 239000003658 microfiber Substances 0.000 description 3
- 210000003632 microfilament Anatomy 0.000 description 3
- 229920000573 polyethylene Polymers 0.000 description 3
- 239000007921 spray Substances 0.000 description 3
- KKEYFWRCBNTPAC-UHFFFAOYSA-L terephthalate(2-) Chemical compound [O-]C(=O)C1=CC=C(C([O-])=O)C=C1 KKEYFWRCBNTPAC-UHFFFAOYSA-L 0.000 description 3
- 238000010438 heat treatment Methods 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 239000000049 pigment Substances 0.000 description 2
- 238000012545 processing Methods 0.000 description 2
- 230000002269 spontaneous effect Effects 0.000 description 2
- VAYOSLLFUXYJDT-RDTXWAMCSA-N Lysergic acid diethylamide Chemical compound C1=CC(C=2[C@H](N(C)C[C@@H](C=2)C(=O)N(CC)CC)C2)=C3C2=CNC3=C1 VAYOSLLFUXYJDT-RDTXWAMCSA-N 0.000 description 1
- 239000011230 binding agent Substances 0.000 description 1
- 238000009835 boiling Methods 0.000 description 1
- 230000015556 catabolic process Effects 0.000 description 1
- 230000000295 complement effect Effects 0.000 description 1
- 230000006835 compression Effects 0.000 description 1
- 238000007906 compression Methods 0.000 description 1
- 238000006731 degradation reaction Methods 0.000 description 1
- 230000004069 differentiation Effects 0.000 description 1
- 239000006185 dispersion Substances 0.000 description 1
- 238000004090 dissolution Methods 0.000 description 1
- 238000001035 drying Methods 0.000 description 1
- 229910001651 emery Inorganic materials 0.000 description 1
- 238000001125 extrusion Methods 0.000 description 1
- 230000004907 flux Effects 0.000 description 1
- 238000001192 hot extrusion Methods 0.000 description 1
- 239000011229 interlayer Substances 0.000 description 1
- 238000009940 knitting Methods 0.000 description 1
- 239000002932 luster Substances 0.000 description 1
- 238000002844 melting Methods 0.000 description 1
- 230000008018 melting Effects 0.000 description 1
- 239000011859 microparticle Substances 0.000 description 1
- 239000012299 nitrogen atmosphere Substances 0.000 description 1
- 230000000704 physical effect Effects 0.000 description 1
- 239000000843 powder Substances 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 238000007790 scraping Methods 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
- 239000002904 solvent Substances 0.000 description 1
- 238000006467 substitution reaction Methods 0.000 description 1
- 229920002994 synthetic fiber Polymers 0.000 description 1
- 239000004758 synthetic textile Substances 0.000 description 1
- 238000012546 transfer Methods 0.000 description 1
- 238000009941 weaving Methods 0.000 description 1
- 230000004580 weight loss Effects 0.000 description 1
Images

Classifications
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H3/00—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length
- D04H3/08—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length characterised by the method of strengthening or consolidating
- D04H3/10—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length characterised by the method of strengthening or consolidating with bonds between yarns or filaments made mechanically
- D04H3/11—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length characterised by the method of strengthening or consolidating with bonds between yarns or filaments made mechanically by fluid jet
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01F—CHEMICAL FEATURES IN THE MANUFACTURE OF ARTIFICIAL FILAMENTS, THREADS, FIBRES, BRISTLES OR RIBBONS; APPARATUS SPECIALLY ADAPTED FOR THE MANUFACTURE OF CARBON FILAMENTS
- D01F8/00—Conjugated, i.e. bi- or multicomponent, artificial filaments or the like; Manufacture thereof
- D01F8/04—Conjugated, i.e. bi- or multicomponent, artificial filaments or the like; Manufacture thereof from synthetic polymers
- D01F8/06—Conjugated, i.e. bi- or multicomponent, artificial filaments or the like; Manufacture thereof from synthetic polymers with at least one polyolefin as constituent
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01F—CHEMICAL FEATURES IN THE MANUFACTURE OF ARTIFICIAL FILAMENTS, THREADS, FIBRES, BRISTLES OR RIBBONS; APPARATUS SPECIALLY ADAPTED FOR THE MANUFACTURE OF CARBON FILAMENTS
- D01F8/00—Conjugated, i.e. bi- or multicomponent, artificial filaments or the like; Manufacture thereof
- D01F8/04—Conjugated, i.e. bi- or multicomponent, artificial filaments or the like; Manufacture thereof from synthetic polymers
- D01F8/12—Conjugated, i.e. bi- or multicomponent, artificial filaments or the like; Manufacture thereof from synthetic polymers with at least one polyamide as constituent
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01F—CHEMICAL FEATURES IN THE MANUFACTURE OF ARTIFICIAL FILAMENTS, THREADS, FIBRES, BRISTLES OR RIBBONS; APPARATUS SPECIALLY ADAPTED FOR THE MANUFACTURE OF CARBON FILAMENTS
- D01F8/00—Conjugated, i.e. bi- or multicomponent, artificial filaments or the like; Manufacture thereof
- D01F8/04—Conjugated, i.e. bi- or multicomponent, artificial filaments or the like; Manufacture thereof from synthetic polymers
- D01F8/14—Conjugated, i.e. bi- or multicomponent, artificial filaments or the like; Manufacture thereof from synthetic polymers with at least one polyester as constituent
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H1/00—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres
- D04H1/40—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties
- D04H1/54—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties by welding together the fibres, e.g. by partially melting or dissolving
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H3/00—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length
- D04H3/005—Synthetic yarns or filaments
- D04H3/007—Addition polymers
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H3/00—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length
- D04H3/005—Synthetic yarns or filaments
- D04H3/009—Condensation or reaction polymers
- D04H3/011—Polyesters
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H3/00—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length
- D04H3/016—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length characterised by the fineness
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H3/00—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length
- D04H3/018—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length characterised by the shape
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H3/00—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length
- D04H3/02—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length characterised by the method of forming fleeces or layers, e.g. reorientation of yarns or filaments
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H3/00—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length
- D04H3/08—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length characterised by the method of strengthening or consolidating
- D04H3/10—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length characterised by the method of strengthening or consolidating with bonds between yarns or filaments made mechanically
- D04H3/105—Non-woven fabrics formed wholly or mainly of yarns or like filamentary material of substantial length characterised by the method of strengthening or consolidating with bonds between yarns or filaments made mechanically by needling
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T442/00—Fabric [woven, knitted, or nonwoven textile or cloth, etc.]
- Y10T442/60—Nonwoven fabric [i.e., nonwoven strand or fiber material]
- Y10T442/608—Including strand or fiber material which is of specific structural definition
- Y10T442/609—Cross-sectional configuration of strand or fiber material is specified
- Y10T442/611—Cross-sectional configuration of strand or fiber material is other than circular
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T442/00—Fabric [woven, knitted, or nonwoven textile or cloth, etc.]
- Y10T442/60—Nonwoven fabric [i.e., nonwoven strand or fiber material]
- Y10T442/608—Including strand or fiber material which is of specific structural definition
- Y10T442/609—Cross-sectional configuration of strand or fiber material is specified
- Y10T442/612—Hollow strand or fiber material
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T442/00—Fabric [woven, knitted, or nonwoven textile or cloth, etc.]
- Y10T442/60—Nonwoven fabric [i.e., nonwoven strand or fiber material]
- Y10T442/608—Including strand or fiber material which is of specific structural definition
- Y10T442/627—Strand or fiber material is specified as non-linear [e.g., crimped, coiled, etc.]
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T442/00—Fabric [woven, knitted, or nonwoven textile or cloth, etc.]
- Y10T442/60—Nonwoven fabric [i.e., nonwoven strand or fiber material]
- Y10T442/637—Including strand or fiber material which is a monofilament composed of two or more polymeric materials in physically distinct relationship [e.g., sheath-core, side-by-side, islands-in-sea, fibrils-in-matrix, etc.] or composed of physical blend of chemically different polymeric materials or a physical blend of a polymeric material and a filler material
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T442/00—Fabric [woven, knitted, or nonwoven textile or cloth, etc.]
- Y10T442/60—Nonwoven fabric [i.e., nonwoven strand or fiber material]
- Y10T442/659—Including an additional nonwoven fabric
- Y10T442/666—Mechanically interengaged by needling or impingement of fluid [e.g., gas or liquid stream, etc.]
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T442/00—Fabric [woven, knitted, or nonwoven textile or cloth, etc.]
- Y10T442/60—Nonwoven fabric [i.e., nonwoven strand or fiber material]
- Y10T442/659—Including an additional nonwoven fabric
- Y10T442/668—Separate nonwoven fabric layers comprise chemically different strand or fiber material
Definitions
- the present invention relates to the field of products textiles and their applications, and relates to a non-woven web of very fine continuous filaments or micro-filaments.
- the present invention aims in particular to widen the field traditional application of nonwovens by giving them properties and physical characteristics plus particularly textile and mechanical, similar to those of woven and knitted textiles, while retaining the advantageous properties and characteristics nonwovens of continuous filaments.
- These known fibers are obtained by techniques of spinning to obtain ultra-fine fibers or microfibers, various sections, and constitution variable polymer. After spinning, these fibers are transformed by known techniques of weaving or knitting and processed using finishing techniques more or less complex.
- An object of the present invention is to obtain products nonwovens with characteristics and properties at least equal to those of woven products or knitted fabrics obtained using the above-mentioned ultra-fine fibers, while clearly applying manufacturing techniques more efficient and less costly, resulting in more great flexibility in terms of the variability of nature and properties of the filaments, methods of consolidation and properties of the products obtained.
- the document US-A-4,239,720 proposes a nonwoven web of a grammage of 100 g / m 2 having a weight proportion PET / PA6 of 80/20.
- the separation of the elementary filaments is obtained after the consolidation of the sheet.
- the elementary filaments are separated from the filament composed by a solvent.
- Document EP-A1-0 455 927 describes the manufacture of nonwoven webs of cut composite fibers, including elementary fibers are separated by dissolution. The production of the tablecloth is only possible by the step additional fiber manufacturing and processing of the last. Microfiber has properties sufficient mechanical strength to withstand the various stages treatment. Separation takes place only if the component "sea" is dissolved.
- Document FR-A-2 705 698 discloses a nonwoven web of a grammage of 110 g / m 2 , which is composed of filaments having a title of 1.5 dTex with two elementary filaments of 50/50 proportion .
- the water table is bound by a jet of water.
- the proportion can vary from 95/5 to 5/95, as well as the grammage between 10 g / m 2 and 400 g / m 2 .
- the invention relates to a method of manufacture of a nonwoven web of continuous filaments, curly or not, obtained by a spinning process direct controlled and formed, after coating, of filaments separable composites and a sheet obtained by this process.
- the subject of the present invention is a method for manufacturing a nonwoven web of continuous filaments bicomponents polyethylene terephthalate / polyamide 6 weight of 120g / m2, with cooling phases, drawing and lapping, uncrimped continuous filaments having a title of 1.6 dTex and presenting in section transverse configuration in orange wedges with a central orifice, said districts or sectors being alternately composed of one of the two materials aforementioned polymers and in direct contact with neighborhoods or adjacent sectors, each composite filament is made up of six elementary polyethylene filaments 0.15 dTex terephthalate and six filaments elementary in polyamide 6 with a titer of 0.11 dTex, resulting in a polyethylene weight proportion terephthalate / polyamide 6 60/40, after coating, the layer aforementioned nonwoven is subjected to the action of jets of pressurized fluid for the separation of filaments' composites in elementary filaments, as well as the entanglement and binding of these.
- Another object of the invention is a nonwoven web of continuous filaments capable of being obtained by separation of the composite continuous filaments, the web being of a grammage of 120 g / m 2 and consisting of continuous non-crimped polyethylene bicomponent filaments terephthalate / polyamide 6, the composite continuous filaments having a titer of 1.6 dTex and having in cross section an orange quarter configuration with a central orifice, said quarters or sectors being alternately composed of one of the two aforementioned polymer materials and in direct contact with the adjacent districts or sectors, each composite filament consisting of six elementary polyethylene terephthalate filaments with a titer of 0.15 dTex and six elementary polyamide 6 filaments with a titer of 0.11 dTex, resulting in a weight ratio of polyethylene terephthalate / polyamide 6 of 60/40, the elementary filaments being entangled and linked.
- Yet another object of the invention is the use of the prescribed tablecloth after dyeing or printing as car interior lining or coating wall.
- Another object of the invention is a nonwoven web according to claim 7, the tablecloth being of a grammage of 130g / m2 characterized in that and the web has been subjected to hot-point calendering and use of the web according to claim 10 or 11 for pigment printing or, after dyeing, as surface coating of vehicle door panels automobiles, coating of injected or molded parts intended to be fitted in the passenger compartments of vehicles, for the production of shoe linings or for making work clothes or after printing for the production of draperies or curtains interior furnishings.
- year may designate the tablecloth obtained as being a nonwoven tablecloth of continuous microfilaments.
- the different polymeric materials forming the filaments composites are divided into separate areas in the cut transverse of these, so as to allow their separation into elementary filaments each corresponding, in cross section, to one of said zones.
- the different polymer materials constituting the composite filaments are advantageously immiscible and / or incompatible between them, due to their nature or following treatment of at least one of said polymeric materials.
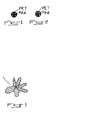
- the composite filaments have, in cross section, a configuration of areas representing the cross sections of different elementary filaments, quarter-shaped orange or Camembert sectors.
- Said districts or sectors, forming the pattern of the cut transverse composite elements may have different dimensions, thus generating, after separation and separation of composite filaments initial, elementary filaments of clearly marked titles different.
- said composite filaments have a longitudinal tubular hollow cavity, centered or not centered with respect to the median axis of said filaments composites.
- this arrangement allows to delete the contact intimate between the edges of the elementary filaments formed by the interior angles of the districts or sectors, before separation of the composite filaments, and contact with it level of different elementary filaments made in one same polymer material.
- the outer contours of the cross sections of composite filaments have a multilobed configuration, defining several sectors or zones each corresponding to an elementary filament.
- the composite filaments can have a latent or spontaneous crimp resulting from asymmetry of behavior of said filaments with respect to their axis longitudinal median, said crimp being activated or accentuated, if necessary, by an asymmetry of the cross section configuration geometry of said composite filaments.
- the composite filaments may have a latent or spontaneous crimp resulting from differentiation physical properties of polymer materials forming the elementary filaments during the operations of spinning, cooling and / or drawing of filaments composites resulting in distortions generated by asymmetrical internal stresses relative to the axis longitudinal median of said composite filaments, said crimp being activated or accentuated, if necessary, by a asymmetry of the geometry of the configuration of the cross section of said composite filaments.
- Composite filaments may have crimp latent which is activated by heat, mechanical treatment or chemical before formation of the nonwoven web.
- Crimp can be accentuated by treatment complementary to the consolidated or unconsolidated sheet, of the type thermal (tunnel oven, boiling water, steam, heating drum, microwave, infrared waves) or chemical type, with possible controlled retraction of the tablecloth.
- the initial composite filaments can be obtained, by example, by electrostatic, mechanical and / or deflection pneumatic (a combination of at least two of these types deflection is possible) and projection on a carpet endless mobile and be mechanically entangled by needling (on one or two sides with needles and under adequate perforation conditions depending properties required for the nonwoven web) or by action of jets of pressurized fluid, whether or not charged with solid micro-particles, possibly after calendering.
- the operations of entanglement and separation of composite filaments into elementary filaments can be carried out in the same process step and with the same device, the more or less complete separation of said elementary filaments which can be completed with a additional operation more targeted on said separation.
- the cohesion and mechanical strength of the nonwoven web can also be significantly increased, by providing for bonding of the elementary filaments with one another by thermofusion of one or more of them formed of a polymer material with a lower melting point, for calendering by means of smooth or engraved heated rollers, by passage in a hot air tunnel oven, by passage on a hot air drum passing through and / or by application of a binding agent contained in a dispersion, in a solution or in powder form.
- the consolidation of the water table can, alternatively, also be made, for example by hot calendering, before any separation of the unitary composite filaments into elementary filaments or micro-filaments, said separation being carried out after consolidation of the water table.
- the structure of said sheet can also be consolidated by chemical treatment (as described by example in French Patent No. 2,546,536 in the name of plaintiff) or thermal resulting in a retraction controlled of at least part of the elementary filaments, after having, if necessary, carried out the separation of these latter, resulting in a retraction of the web in the width and / or lengthwise.
- the nonwoven web may be subjected, after consolidation, binding or finishing treatment chemical type, such as anti-pilling treatment, hydrophylizing, anti-static, improving resistance to fire and / or modification of touch or luster, of the mechanical type, such as scraping, sanforization, emery or passage through a tumbler, and / or of the type modifying the external appearance such as the dyeing or printing.
- chemical type such as anti-pilling treatment, hydrophylizing, anti-static, improving resistance to fire and / or modification of touch or luster
- the mechanical type such as scraping, sanforization, emery or passage through a tumbler
- the type modifying the external appearance such as the dyeing or printing.
- a sheet of two-component continuous filaments is produced polyethylene terephthalate / polyamide 6.
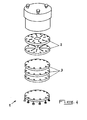
- the unit of wiring 1 consists of two chambers, one of which is located in the axis of said unit (PA6 wiring) and whose the second, of annular shape, surrounds the first (spinning PET).
- the two distribution plates allow distribution both circular and radial.
- the stack of the three final distribution plates allows alveolar feeding of each of the holes the sector.
- Each of said holes thus has its own own power circuit and allows you to spin a unitary composite filament.
- the die itself is made up of 180 holes 0.28 mm diameter and 0.56 mm long capillaries. A schematic representation of an orifice of such a die is reproduced in Figure 6 of the accompanying drawings.
- the extrusion temperatures of the two polymers are 295 ° C for PET and 255 ° C respectively for PA6, the spinning boat itself being one temperature of 278 ° C, the spinning speed is about 4 500 m / 60s and the flow rate per die hole of 0.7 g / 60s (0.35 g / 60s per polymer).
- the drying of PA6 and the feeding of the extruder are carried out under a nitrogen atmosphere and the transfer circuits polymers to the die are designed in such a way so that the residence and routing times of said polymers are short enough to avoid any significant degradation of the latter.
- the nonwoven web obtained has a grammage of 120 g / m2 and is made up of uncrimped continuous filaments having a titer of 1.6 dTex and presenting in cross section a orange wedge configuration with an orifice central, said districts or sectors being composed alternatively of one of the two polymer materials mentioned above and in direct contact with the districts or adjacent sectors (section structure comparable to that shown in Figure 2 of the accompanying drawings).
- Each composite filament consists of six filaments elementary polyethylene terephthalate with a title of 0.15 dTex and six elementary polyamide 6 filaments 0.11 dTex, resulting in a proportion weight polyethylene terephthalate / polyamide 6 of 60/40.
- the aforementioned non-woven fabric is subjected to the action of jets of fluid (water) under pressure in order to separate the composite filaments by elementary filaments, as well as the entanglement and the binding of these.
- said hydraulic binding consists, successively, in one pass of the nonwoven web under a first mooring ramp, in a spin of the water table wet (by passing between two pressure rollers or by suction, for example) and finally in a Passage of the tablecloth at the level of the three successive sets of tying hydraulic on suction drum, said assemblies acting respectively on the front, back and front sides of the tablecloth and each comprising three bars or lines jets spaced 0.6 mm apart.
- the nonwoven web moves on an 80 mesh metallic canvas (80 thread / 2.54 cm) with 70% opening.
- Read speed processing in this case is around 15m / 60s.
- the conditions for adjusting the aforementioned hydraulic tying assemblies are as follows 1st set - Face RECTO Spray line Line 1 Line 2 Line 3 Nozzle diameter ( ⁇ ) 100 100 100 Pressure (bars) 120 180 180 2nd set - Face RECTO Spray line Line 1 Line 2 Line 3 Nozzle diameter ( ⁇ ) 120 120 120 Pressure (bars) 230 230 230 3rd set - Face RECTO Spray line Line 1 Line 2 Line 3 Nozzle diameter ( ⁇ ) 120 120 120 Pressure (bars) 230 230 230 230 230 230 230 230 230 230
- the nonwoven web is wrung out by compression between two pressure rollers, dried on a through air drum heated to 160 ° C and finally wound.
- This tablecloth has special characteristics and properties: appearance and texture of a fabric of the "flannel” type, breaking load and high tear resistance, good drapability and good abrasion resistance.
- the sheet obtained by the aforementioned process, in fact forming a non-woven fabric can be advantageously used, after dyeing or printing and possibly embossing at hot, as an interior covering for a car roof or wall covering.
- a nonwoven web of continuous filaments is produced according to a process similar to that described in Example 1, said ply being subjected to an identical hydraulic binding to that described above.
- the tablecloth obtained however, has a grammage of 130 g / m2 and is subjected, following the hydraulic tying, to a dot calendering using two metal rollers heated, namely a roll engraved at 232 ° C and a roll smooth at 215 ° C (pressing force: 50daN / cm in width; speed: 15m / min; 52 points / cm2; area percentage linked: 13%).
- the tablecloth obtained may be advantageously used for pigment printing or, after dyeing, as surface coating of vehicle door panels automobiles, coating of injected or molded parts intended to be fitted in the passenger compartments of vehicles, for the production of shoe linings or for the production of work clothes.
- said tablecloth can also be used, after printing (in particular of the "fixed-washed” type), for the production of drapes or drapes inside.
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- General Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Nonwoven Fabrics (AREA)
- Multicomponent Fibers (AREA)
- Spinning Methods And Devices For Manufacturing Artificial Fibers (AREA)
Description
- composante apparente des éléments de revêtement intérieur des véhicules automobiles,
- textile pour l'ameublement intérieur et extérieur,
- textile pour la fabrication des dessus de doublures et des couches intercalaires de composants de chaussures et
- textile pour la fabrication de pièces de vêtements ou de doublures de pièces de vêtements.

- deux plaques de répartition 2 destinées à croiser les flux des deux chambres.
- trois plaques 3 dédiées à la distribution proprement dite.
| 1er ensemble - Face RECTO | |||
| Ligne de jets | Ligne 1 | Ligne 2 | Ligne 3 |
| Diamètre buses (µ) | 100 | 100 | 100 |
| Pression (bars) | 120 | 180 | 180 |
| 2ème ensemble - Face RECTO | |||
| Ligne de jets | Ligne 1 | Ligne 2 | Ligne 3 |
| Diamètre buses (µ) | 120 | 120 | 120 |
| Pression (bars) | 230 | 230 | 230 |
| 3ème ensemble - Face RECTO | |||
| Ligne de jets | Ligne 1 | Ligne 2 | Ligne 3 |
| Diamètre buses (µ) | 120 | 120 | 120 |
| Pression (bars) | 230 | 230 | 230 |
| Mesure | Unité | Méthode | Exemple 1 | Exemple 2 |
| Masse surfacique | g/m2 | NFG 38013 | 120 | 130 |
| Epaisseur | mm | NFG 38012 | 0,63 | 0,55 |
| Charge rup- tune sL/sT | DaN/5cm | NFG 07001 | 43,0/32,0 | 38,0!25,7 |
| Isotropie | - | 1,34 | 1,48 | |
| Allongement sL/sT | % | NFG 07001 | 73/85 | 56,2/72,8 |
| Charge 3 % sL/sT | daN/5cm | NFG 07001 | 2,110,55 | 5,52/0,98 |
| Charge 5 % sL/sT | daN/5cm | NFG 07001 | 3,5/0,87 | 8,1/1,6 |
| Charge 15 % sL/sT | daN/5cm | NFG 07001 | 10,8/3,2 | 16,7/5,15 |
| Energie rupture sL/sT | J | NFG 07001 | 41,5/25,3 | 28,8/19,2 |
| Retrait thermique sL/sT | % | 180° -15mn | -0,6/-0,4 | -1,5/0,2 |
| MasseCV%(5 x5cm) | % | 3,7 | 3,0 | |
| Déchirure amorcée sL/sT | daN | NFG 07146 | 2,4/3,6 | 1,8/3,4 |
| Charge spécifique [(L + T)/2] / masse surfacique | daN/g/m2 | 3,1 | 2,45 | |
| Module initial calc. ?1m (tangente charge à 3 %) | MN/m | 4,1 | 11,0 | |
| Résistance à l'abrasion (9kPa) Perte en Charge | Nombre de cycle % | Martindale ITF BS 5690 | 50.000 - 10,5 | 50.000 - 6,6 |
| Porosité (5cm - 196 Pa) | l/m2s | NFG 07111 | 555 | 272 |
| Coefficient de drapé | NFG 07109 | 0,91 | 0,82 |
Claims (12)
- Procédé de fabrication d'une nappe non-tissée de filaments continus bicomposés polyéthylène térephtalate/polyamide 6 d'un grammage de 120g/m2, avec des phases de refroidissement, d'étirage et de nappage, de filaments continus non frisés ayant un titre de 1,6 dTex et présentant en coupe transversale une configuration en quartiers d'orange avec un orifice central, lesdits quartiers ou secteurs étant composés alternativement de l'un des deux matériaux polymères précités et en contact direct avec les quartiers ou secteurs adjacents, chaque filament composite étant constitué de six filaments élémentaires en polyéthylène térephtalate d'un titre de 0,15 dTex et de six filaments élémentaires en polyamide 6 d'un titre de 0,11 dTex, aboutissant à une proportion pondérale polyéthylène térephtalate/polyamide 6 de 60/40, et après nappage, la nappe non-tissée précitée est soumise à l'action de jets de fluide sous pression en vue de réaliser la séparation des filaments composites en filaments élémentaires, ainsi que l'enchevêtrement et le liage de ces derniers.
- Procédé, de fabrication d'une nappe non-tissée de filaments continus selon la revendication 1, caractérisé en ce que la nappe est soumise, consécutivement au liage hydraulique, à un calandrage par points au moyen de deux rouleaux métalliques chauffés résultant à une nappe d'un grammage de 130g/m2.
- Procédé selon la revendication 2, caractérisé en ce qu'un rouleau gravé est à 232 °C et un rouleau lisse est à 215°C et en ce que la force pressante est 50daN/cm de largeur avec une vitesse de 15m/min et 52 points/cm2, le pourcentage de surface liée étant de 13 %.
- Procédé selon l'une des revendications 1 à 3, caractérisé en ce que ledit liage hydraulique consiste, successivement, en un passage de la nappe non-tissée sous une première rampe de mouillage, en un essorage de la nappe mouillée et enfin en un passage de la nappe au niveau de trois ensembles successifs de liage hydraulique sur tambour aspirant.
- Procédé selon la revendication 4, caractérisé en ce que lesdits ensembles agissent respectivement sur les faces recto, verso et recto de la nappe et comportent chacun trois barrettes ou lignes de jets.
- Procédé selon la revendication 5, caractérisé par des conditions de réglage des ensembles de liage hydraulique pression suivantes:1er ensemble - face RECTO
Ligne de jets Ligne 1 Ligne 2 Ligne 3 Diamètre buses (µm) 100 100 100 Pression (bar) 120 180 180 2ème ensemble - face VERSOLigne de jets Ligne 1 Ligne 2 Ligne 3 Diamètre buses (µm) 120 120 120 Pression (bars) 230 230 230 3ème ensemble - face RECTOLigne de jets Ligne 1 Ligne 2 Ligne 3 Diamètre buses (µm) 120 120 120 Pression (bars) 230 230 230. - Nappe non-tissée de filaments continus susceptibles d'être obtenus par séparation des filaments continus composites, la nappe étant d'un grammage de 120g/m2 et étant constitutée de filaments continus non frisés bicomposés polyéthylène térephtalate/polyamide 6, les filaments continus composites ayant un titre de 1,6 dTex et présentant en coupe transversale une configuration en quartiers d'orange avec un orifice central, lesdits quartiers ou secteurs étant composés alternativement de l'un des deux matériaux polymères précités et en contact direct avec les quartiers ou secteurs adjacents, chaque filament composite étant constitué de six filaments élémentaires en polyéthylène térephtalate d'un titre de 0,15 dTex et de six filaments élémentaires en polyamide 6 d'un titre de 0,11 dTex, aboutissant à une proportion pondérale polyéthylène térephtalate/polyamide 6 de 60/40, les filaments élémentaires étant enchevêtrés et liés.
- Utilisation de la nappe selon la revendication 7 après teinture ou impression en tant que revêtement intérieur pour pavillon automobile ou revêtement mural.
- Utilisation de la nappe selon la revendication 8 après gaufrage à chaud en tant que revêtement intérieur pour pavillon automobile ou revêtement mural.
- Nappe non-tissée de filaments continus selon la revendication 7, la nappe étant d'un grammage de 130g/m2, caractérisé en ce que la nappe a été soumise à un calandrage par points à chaud.
- Nappe non-tissée de filaments continus selon la revendication 10, caractérisé en ce que le pourcentage de surface liée de la nappe est de 13 %.
- Utilisation de la nappe selon la revendication 10 ou 11 pour l'impression pigmentaire ou, après teinture, en tant que revêtement apparent de panneaux de portières de véhicules automobiles, revêtement de pièces injectées ou moulées destinées à être montées dans les habitacles des véhicules, pour la fabrication de doublures intérieures de chaussures ou pour la fabrication de vêtements de travail ou après impression pour la réalisation de tentures ou de rideaux d'ameublement intérieur.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9607659 | 1996-06-17 | ||
| FR9607659A FR2749860B1 (fr) | 1996-06-17 | 1996-06-17 | Nappe non tissee formee de filaments continus tres fins |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0814188A1 EP0814188A1 (fr) | 1997-12-29 |
| EP0814188B1 true EP0814188B1 (fr) | 2003-09-24 |
Family
ID=9493239
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP97108364A Expired - Lifetime EP0814188B1 (fr) | 1996-06-17 | 1997-05-23 | Nappe nontissée formée de filaments continus très fins |
Country Status (10)
| Country | Link |
|---|---|
| US (1) | US5899785A (fr) |
| EP (1) | EP0814188B1 (fr) |
| JP (1) | JPH1053948A (fr) |
| CN (1) | CN1093191C (fr) |
| BR (1) | BR9703602A (fr) |
| CA (1) | CA2208117C (fr) |
| DE (1) | DE69725051T2 (fr) |
| FR (1) | FR2749860B1 (fr) |
| TW (1) | TW348192B (fr) |
| ZA (1) | ZA975216B (fr) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102004036099A1 (de) * | 2004-07-24 | 2006-03-16 | Carl Freudenberg Kg | Mehrpomponenten-Spinnvliesstoff, Verfahren zu seiner Herstellung sowie Verwendung der Mehrkomponenten-Spinnvliesstoffe |
| EP1891871A2 (fr) | 2006-08-26 | 2008-02-27 | Bleuel, Norbert | Dispositif de polissage, de nettoyage ou de séchage de l'intérieur d'un récipient pour recevoir des liquides |
| DE102007041630A1 (de) | 2007-09-03 | 2009-03-05 | Carl Freudenberg Kg | Verfahren zur Herstellung eines Flächengebildes aus zumindest teilweise gesplitteten Garnen, Fasern oder Filamenten und Vorrichtung zu dessen Herstellung |
| WO2012155980A1 (fr) * | 2011-05-19 | 2012-11-22 | Gardena Manufacturing Gmbh | Conduite d'eau pour système d'arrosage de plantes et système d'arrosage de plantes |
Families Citing this family (135)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB9626636D0 (en) | 1996-12-21 | 1997-02-12 | British United Shoe Machinery | Lining material |
| FR2779746B1 (fr) * | 1998-06-11 | 2000-07-21 | Novalis Fibres | Utilisation de fibres a frisure tridimensionnelle pour la fabrication de tissu ou toile de renfort, et tissu de renfort obtenu |
| US6225243B1 (en) * | 1998-08-03 | 2001-05-01 | Bba Nonwovens Simpsonville, Inc. | Elastic nonwoven fabric prepared from bi-component filaments |
| US20060252332A9 (en) * | 1998-09-14 | 2006-11-09 | Ortega Albert E | Nonwoven fabrics with two or more filament cross sections |
| ATE298016T1 (de) * | 1998-09-14 | 2005-07-15 | Cerex Advanced Fabrics Inc | Vliessstoffe |
| FR2790487B1 (fr) * | 1999-03-02 | 2001-04-20 | Freudenberg Carl Fa | Procede de fabrication de filaments ou de fibres multisegmente(e)s, ainsi que filaments ou fibres et surface textile resultants |
| FR2790489B1 (fr) * | 1999-03-01 | 2001-04-20 | Freudenberg Carl Fa | Nappe non tissee en filaments ou fibres thermolie(e)s |
| US7091140B1 (en) | 1999-04-07 | 2006-08-15 | Polymer Group, Inc. | Hydroentanglement of continuous polymer filaments |
| DE19934442C2 (de) * | 1999-07-26 | 2001-09-20 | Freudenberg Carl Fa | Verfahren zur Herstellung eines Vliesstoffs und Vliesstoff zur Herstellung von Reinraum-Schutzbekleidung |
| ITMI990561U1 (it) * | 1999-09-09 | 2001-03-09 | Emilio Mina | Struttura di accappatoio confezionato con un tessuto non tessuto realizzato in microfibra |
| DE19947870C1 (de) * | 1999-10-05 | 2001-05-10 | Freudenberg Carl Fa | Fersenfutter für die Schuhindustrie |
| DE19947869A1 (de) | 1999-10-05 | 2001-05-03 | Freudenberg Carl Fa | Synthetisches Leder |
| DE19960063C2 (de) * | 1999-12-13 | 2002-03-14 | Freudenberg Carl Kg | Innenfutter für die Schuhindustrie |
| DE19962356A1 (de) * | 1999-12-23 | 2001-07-05 | Freudenberg Carl Fa | Sanitärwäsche |
| DE19962359B4 (de) * | 1999-12-23 | 2004-07-08 | Carl Freudenberg Kg | Thermovliesstoff |
| DE19962358C1 (de) * | 1999-12-23 | 2001-04-26 | Freudenberg Carl Fa | Taschenfutterstoff |
| DE19962360B4 (de) * | 1999-12-23 | 2005-06-30 | Carl Freudenberg Kg | Arbeitsschutzbekleidung |
| DE19962355A1 (de) * | 1999-12-23 | 2001-07-05 | Freudenberg Carl Fa | Sanitärbekleidung |
| DE19962361A1 (de) * | 1999-12-23 | 2001-07-12 | Freudenberg Carl Fa | Sportbekleidung |
| DE19962357A1 (de) * | 1999-12-23 | 2001-07-05 | Freudenberg Carl Fa | Schlafbekleidung |
| DE19962313C1 (de) * | 1999-12-23 | 2001-04-19 | Freudenberg Carl Fa | Schlafwäsche |
| US6655633B1 (en) * | 2000-01-21 | 2003-12-02 | W. Cullen Chapman, Jr. | Tubular members integrated to form a structure |
| DE10002778B4 (de) * | 2000-01-22 | 2012-05-24 | Robert Groten | Verwendung eines Mikrofilament-Vliesstoffes als Reinigungstuch |
| DE10009281C1 (de) * | 2000-02-28 | 2001-03-22 | Freudenberg Carl Fa | Schallabsorptionsmaterial |
| DE10009283C2 (de) * | 2000-02-28 | 2002-02-21 | Freudenberg Carl Kg | Airbagschutzhülle |
| DE10011053C2 (de) * | 2000-03-07 | 2002-06-20 | Freudenberg Carl Kg | Textiles Lichtschutzmaterial |
| US6692541B2 (en) | 2000-05-16 | 2004-02-17 | Polymer Group, Inc. | Method of making nonwoven fabric comprising splittable fibers |
| US6702063B1 (en) * | 2000-05-25 | 2004-03-09 | Aica Engineering Co. Ltd. | Surface material and method of suppressing influence of surface wave |
| DE10026281B4 (de) * | 2000-05-26 | 2005-06-02 | Sächsisches Textilforschungsinstitut e.V. | Verfahren zur Herstellung von Spinnvliesen |
| US6743273B2 (en) | 2000-09-05 | 2004-06-01 | Donaldson Company, Inc. | Polymer, polymer microfiber, polymer nanofiber and applications including filter structures |
| WO2002077332A1 (fr) * | 2001-03-26 | 2002-10-03 | Carl Freudenberg Kg | Dispositif pour produire des fils, des fibres ou des filaments pouvant etre separes |
| DE10115185A1 (de) * | 2001-03-27 | 2002-10-24 | Freudenberg Carl Kg | Splittfähige Garne, Fasern oder Filamente und Verfahren zu deren Herstellung sowie Vorrichtung |
| WO2002097187A1 (fr) * | 2001-05-25 | 2002-12-05 | Carl Freudenberg Kg | Procede pour reduire le boulochage |
| DE10133769A1 (de) * | 2001-05-25 | 2002-12-05 | Freudenberg Carl Kg | Verfahren zur Reduzierung des Pillings |
| DE10127471A1 (de) * | 2001-06-07 | 2002-12-12 | Fleissner Gerold | Verfahren zur Herstellung eines verfestigten Nonwoven aus zumindest teilweise mikrofeinen Endlosfilamenten und Nonwoven nach diesem Verfahren |
| DE10129366B4 (de) * | 2001-06-20 | 2009-06-10 | Freudenberg, Carl | Mit Pigmenten gefärbter und/oder bedruckter Vliesstoff, Verfahren zu dessen Herstellung und diese umfassende Textilien |
| DE10135940B4 (de) * | 2001-07-24 | 2008-10-23 | Carl Freudenberg Kg | Verfahren zur Herstellung gefärbter und/oder bedruckter Vliesstoffe und deren Verwendung |
| DE10135941A1 (de) * | 2001-07-24 | 2003-02-13 | Freudenberg Carl Kg | Verfahren zum Färben und/oder Bedrucken von textilem Material |
| JP4646462B2 (ja) * | 2001-08-10 | 2011-03-09 | 日本ケミコン株式会社 | 電解コンデンサ |
| US20040216828A1 (en) * | 2001-08-17 | 2004-11-04 | Ortega Albert E. | Nonwoven fabrics with two or more filament cross sections |
| EP1438452A1 (fr) * | 2001-08-17 | 2004-07-21 | Cerex Advanced Fabrics, Inc. | Non-tisses a un ou des sections de filaments |
| US20030153229A1 (en) * | 2002-02-08 | 2003-08-14 | Mcdaniel John Scott | Fabric made from conjugate yarns having enhanced absorbency |
| US20030157854A1 (en) * | 2002-02-08 | 2003-08-21 | Miller Brian C. | Chemically modified nonwoven articles and method for producing the same |
| US6602437B1 (en) | 2002-02-08 | 2003-08-05 | Millikien & Company | Chemically modified nonwoven articles and method for producing the same |
| US6673125B2 (en) | 2002-02-08 | 2004-01-06 | Milliken & Company | Chemically modified nonwoven articles and method for producing the same |
| US6863697B2 (en) | 2002-02-08 | 2005-03-08 | Milliken & Company | Process for enhancing the absorbency of a fabric having conjugate yarns |
| WO2003066959A1 (fr) * | 2002-02-08 | 2003-08-14 | Milliken & Company | Articles non tisses chimiquement modifies et procede de production associe |
| US6812172B2 (en) * | 2002-02-12 | 2004-11-02 | Milliken & Company | Microdenier fabric having enhanced dyed appearance |
| US6689175B2 (en) | 2002-02-12 | 2004-02-10 | Milliken & Company | Process for enhancing the dyed appearance of a microdenier fabric |
| WO2003069046A2 (fr) * | 2002-02-12 | 2003-08-21 | Milliken & Company | Procede permettant d'ameliorer l'aspect d'un tissu a microdeniers, et produit resultant |
| US6715189B2 (en) | 2002-02-27 | 2004-04-06 | Milliken & Company | Method for producing a nonwoven fabric with enhanced characteristics |
| US20030162459A1 (en) * | 2002-02-27 | 2003-08-28 | Osbon Robert Lindsay | Method for producing a nonwoven fabric with enhanced characteristics |
| US20030176135A1 (en) * | 2002-03-15 | 2003-09-18 | Wenstrup Dave E. | Method for producing a spun-bonded nonwoven web with improved abrasion resistance |
| US6720278B2 (en) * | 2002-03-15 | 2004-04-13 | Milliken & Company | Method for producing a spun-bonded nonwoven web with improved abrasion resistance |
| US7201777B2 (en) * | 2002-03-28 | 2007-04-10 | Booker Jr Archer E D | Nonwoven fabric having low ion content and method for producing the same |
| US20030186609A1 (en) * | 2002-03-28 | 2003-10-02 | Booker Archer E. D. | Nonwoven fabric having low ion content and method for producing the same |
| US20030199219A1 (en) * | 2002-04-19 | 2003-10-23 | Hayes Heather J. | Patterned nonwoven fabric |
| US20030199220A1 (en) * | 2002-04-22 | 2003-10-23 | Dawson Durwin Glann | Nonwoven fabric having three-dimensional printed surface and method for producing the same |
| WO2003089706A1 (fr) * | 2002-04-22 | 2003-10-30 | Milliken & Company | Non tisse a surface tridimensionnelle imprimee et procede pour le produire |
| US6737114B2 (en) * | 2002-04-22 | 2004-05-18 | Milliken & Company | Nonwoven fabric having three-dimensional printed surface and method for producing the same |
| DE10219929A1 (de) * | 2002-05-03 | 2003-12-04 | Freudenberg Carl Kg | Verfahren zur Verbesserung von Weichheit und/oder Fall von Vliesstoffen |
| US6881111B2 (en) * | 2002-07-30 | 2005-04-19 | Werner Paddles | Shaft coupler with positive angular and axial locking features for coupling paddle sections together and angularly positioning the sections relative to each other |
| EP1396567B2 (fr) † | 2002-08-09 | 2011-04-20 | Reifenhäuser GmbH & Co. KG Maschinenfabrik | Procédé de fabrication d'une nappe non-tissé de filaments bicomposés |
| CA2503049A1 (fr) * | 2002-10-24 | 2004-05-06 | Advanced Design Concept Gmbh | Fibres multicomposants elastomeres, bandes et toiles non tissees |
| US20030146346A1 (en) * | 2002-12-09 | 2003-08-07 | Chapman Jr W. Cullen | Tubular members integrated to form a structure |
| DE10258112B4 (de) * | 2002-12-11 | 2007-03-22 | Carl Freudenberg Kg | Verfahren zur Herstellung eines Flächengebildes aus zumindest teilweise gesplitteten Garnen, Fasern oder Filamenten |
| US6808786B2 (en) * | 2003-02-04 | 2004-10-26 | Freudenberg Nonwovens | Automotive tufted carpet with enhanced acoustical properties |
| US7045211B2 (en) * | 2003-07-31 | 2006-05-16 | Kimberly-Clark Worldwide, Inc. | Crimped thermoplastic multicomponent fiber and fiber webs and method of making |
| US7842306B2 (en) | 2003-08-14 | 2010-11-30 | Milliken & Company | Wound care device having fluid transfer properties |
| US7118761B2 (en) | 2003-08-14 | 2006-10-10 | Canada T Andrew | Method for producing a silver-containing wound care device |
| US8563447B2 (en) * | 2003-08-14 | 2013-10-22 | Milliken & Company | Silver-containing wound care device |
| US20050147657A1 (en) * | 2003-08-14 | 2005-07-07 | Milliken & Company | White silver-containing wound care device |
| US20050037057A1 (en) * | 2003-08-14 | 2005-02-17 | Schuette Robert L. | Silver-containing antimicrobial fabric |
| US20050035327A1 (en) * | 2003-08-14 | 2005-02-17 | Canada T. Andrew | Topical silver-based antimicrobial composition for wound care devices |
| US8017145B2 (en) * | 2003-12-22 | 2011-09-13 | Conopco, Inc. | Exfoliating personal care wipe article containing an array of projections |
| DE102004006373B4 (de) * | 2004-02-09 | 2014-12-31 | Reifenhäuser GmbH & Co Maschinenfabrik | Verfahren zur Herstellung eines Spinnvlieses aus Filamenten |
| DE102004060105A1 (de) * | 2004-04-19 | 2006-01-26 | Sefar Ag | Flächenstück zur Aufnahme eines Druckmusters, Verfahren zu dessen Herstellung sowie seine Verwendung |
| JP2006021030A (ja) * | 2004-06-07 | 2006-01-26 | Japan Vilene Co Ltd | ダウンプルーフ構造体 |
| GB2415011B (en) * | 2004-06-11 | 2009-01-14 | Louver Lite Ltd | Blind fabric |
| JP4602001B2 (ja) * | 2004-06-17 | 2010-12-22 | 株式会社クラレ | 極細長繊維絡合シートの製造方法 |
| US8178184B2 (en) | 2004-06-17 | 2012-05-15 | Kuraray Co., Ltd. | Process for producing intertwined ultrafine filament sheet |
| DE602005004234T2 (de) * | 2004-11-10 | 2009-01-08 | Carl Freudenberg Kg | Dehnbare Vliesstoffe |
| WO2006055842A1 (fr) * | 2004-11-18 | 2006-05-26 | Precision Fabrics Group, Inc. | Procedes d'appretage de tissus barrieres medicaux |
| DE102005014317A1 (de) | 2005-03-30 | 2006-10-05 | Carl Freudenberg Kg | Synthetisches Leder, Verfahren zu dessen Herstellung und dessen Verwendung |
| ES2570965T3 (es) * | 2005-06-24 | 2016-05-23 | Univ North Carolina State | Tejidos de micro y nanofibras duraderos, de alta resistencia, producidos fibrilando islas bicomponentes en el mar de fibras |
| DE102005054726A1 (de) | 2005-08-02 | 2007-02-15 | Carl Freudenberg Kg | Vliesstoffe und Verfahren zu deren Herstellung |
| WO2007016498A2 (fr) * | 2005-08-02 | 2007-02-08 | Raytech Composites, Inc. | Tampons de polissage non-tissés pour polissage mécanico-chimique |
| WO2007112443A2 (fr) * | 2006-03-28 | 2007-10-04 | North Carolina State University | Tissu non tissé de microfibres et de nanofibres par filage direct |
| DE202006014252U1 (de) * | 2006-06-09 | 2008-02-21 | Bleuel, Norbert | Vorrichtung zum Reinigen von Böden |
| AU2007315535B2 (en) | 2006-10-11 | 2011-10-20 | Toray Industries, Inc. | Leather-like sheet and process for production thereof |
| JP5009056B2 (ja) * | 2007-06-06 | 2012-08-22 | 日本バイリーン株式会社 | ダウンプルーフ構造体 |
| DE102007040795B4 (de) | 2007-08-28 | 2011-06-09 | Carl Freudenberg Kg | Verwendung eines Flächengebildes |
| ATE433510T1 (de) * | 2007-09-20 | 2009-06-15 | Freudenberg Carl Kg | Velournadelvliesstoff und seine verwendung |
| DE102008015053A1 (de) | 2008-03-19 | 2009-09-24 | Carl Freudenberg Kg | Antibakteriell ausgerüstetes Vlies mit Bikomponetenfasern |
| EP2103724B1 (fr) | 2008-03-19 | 2011-06-08 | Carl Freudenberg KG | Chiffon doté d'un tissu non tissé antibactérien |
| DE102008053528A1 (de) | 2008-10-28 | 2010-04-29 | Carl Freudenberg Kg | Flachdichtung |
| US20110039468A1 (en) | 2009-08-12 | 2011-02-17 | Baldwin Jr Alfred Frank | Protective apparel having breathable film layer |
| DE202009018620U1 (de) | 2009-08-31 | 2012-05-02 | Norbert Bleuel | Reinigungsbezug |
| DE202011005643U1 (de) | 2011-04-27 | 2011-10-07 | Carl Freudenberg Kg | Waschelement für Fahrzeugwaschanlage |
| EP3238531B1 (fr) | 2011-05-19 | 2019-02-13 | Husqvarna AB | Conduite d'eau pour l'arrosage par capillarité dans un système d'arrosage de plantes |
| US8978997B2 (en) * | 2012-02-13 | 2015-03-17 | Fabrictech 2000, Llc | Aromatic cover |
| DE102012002954B4 (de) | 2012-02-16 | 2015-07-02 | Carl Freudenberg Kg | Verwendung eines Mikrofilament-Vliesstoffs als textiles UV-Lichtschutzmaterial |
| EP2650428A3 (fr) | 2012-04-15 | 2015-09-16 | Norbert Bleuel | Enveloppe de nettoyage |
| DE102012018852B4 (de) | 2012-09-25 | 2016-01-07 | Carl Freudenberg Kg | Verwendung von Mikrofaser-Vliesstoffen zur Herstellung dekorativer Schichtpressstoffe |
| JP6173670B2 (ja) * | 2012-10-03 | 2017-08-02 | ダイワボウホールディングス株式会社 | フィルターおよびその製造方法 |
| CN102922871A (zh) * | 2012-11-21 | 2013-02-13 | 吴江征明纺织有限公司 | 一种印花直热装置 |
| US9834864B2 (en) * | 2013-02-26 | 2017-12-05 | Mitsubishi Chemical Corporation | Process for producing a fibrous bundle via a spinning nozzle |
| CN104695137A (zh) * | 2013-12-04 | 2015-06-10 | 上海杰事杰新材料(集团)股份有限公司 | 一种抗静电无纺布及其制备方法 |
| ES2805798T3 (es) | 2014-04-11 | 2021-02-15 | Hydroflex Group GmbH | Mopa plana, en particular mopa plana de un solo uso |
| US10744435B2 (en) | 2014-07-30 | 2020-08-18 | Sabic Global Technologies B.V. | Spunbond polycarbonate resin filter media |
| CN105063847B (zh) * | 2015-08-11 | 2016-03-30 | 福建省百凯弹性织造有限公司 | 一种具有收纳空间的织带 |
| EP3165654A1 (fr) | 2015-11-09 | 2017-05-10 | Carl Freudenberg KG | Utilisation de non-tisse a filament continu destine a retenir les plumes dans des produits textiles remplis de plumes |
| EP3216905B1 (fr) * | 2016-03-10 | 2019-07-03 | Reifenhäuser GmbH & Co. KG Maschinenfabrik | Matiere non tissee pouvant etre soudee, procede de fabrication d'une matiere non tissee et emballage |
| KR20170113435A (ko) | 2016-04-01 | 2017-10-12 | 코오롱인더스트리 주식회사 | 마스크 팩용 부직포 시트 |
| ES2794010T3 (es) * | 2016-05-18 | 2020-11-17 | Fibertex Personal Care As | Método para hacer una banda no tejida de curvatura alta |
| DE102016010163A1 (de) | 2016-08-25 | 2018-03-01 | Carl Freudenberg Kg | Technisches Verpackungsmaterial |
| CN110198837B (zh) * | 2017-01-23 | 2023-03-31 | 奥斯龙明士克公司 | 透气性屏障织物及其制造方法、洁净室服装 |
| GB201712165D0 (en) * | 2017-07-28 | 2017-09-13 | Smith & Nephew | Wound dressing and method of manufacture |
| CN108589053A (zh) * | 2018-03-13 | 2018-09-28 | 苏州多瑈新材料科技有限公司 | 一种双组分中空纺粘非织造物制造方法 |
| BR112021025410A2 (pt) * | 2019-07-18 | 2022-02-01 | Essity Hygiene & Health Ab | Material de folha, processo de produção de material de folha, pano e uso de material de folha |
| CN110894622B (zh) * | 2019-11-06 | 2022-01-28 | 青岛大学 | 粘结强度可控的类橘瓣形结构复合纤维及其制备工艺 |
| CN110923847A (zh) * | 2019-11-06 | 2020-03-27 | 芦山华美包纱有限公司 | 一种高弹热熔的复合异型纤维及其制备工艺 |
| EP3912687A1 (fr) | 2020-05-20 | 2021-11-24 | Carl Freudenberg KG | Masque facial pourvu de moyen de filtrage à filaments à composants multiples |
| US11541829B2 (en) | 2020-06-18 | 2023-01-03 | Freudenberg Performance Materials Lp | Acoustical baffle |
| CN111763997A (zh) * | 2020-07-16 | 2020-10-13 | 常州纺兴精密机械有限公司 | 三组份复合中空纤维及其纺丝组件 |
| EP4088602A1 (fr) | 2021-05-12 | 2022-11-16 | Carl Freudenberg KG | Masque facial avec milieu filtrant à partir de filaments multicomposant clivés et fibres obtenues par extrusion soufflage |
| EP4108820B1 (fr) | 2021-06-21 | 2025-03-05 | Carl Freudenberg KG | Sac alimentaire non-tissé fabriqué à partir de filaments multicomposants |
| CN114351361A (zh) * | 2021-12-08 | 2022-04-15 | 杭州叙源无纺布制品有限公司 | 一种纳米缓释无纺布的制造方法 |
| US12258692B2 (en) * | 2022-03-01 | 2025-03-25 | Elc Management Llc | Cosmetic sheet masks for improved product delivery |
| CN114892292A (zh) * | 2022-06-14 | 2022-08-12 | 绍兴山海纺织有限公司 | 一种复合fdy长丝 |
| CN121969496A (zh) | 2023-08-07 | 2026-05-01 | 科德宝两合公司 | 非织造复合织物 |
| EP4592072B1 (fr) | 2024-01-24 | 2026-04-15 | Carl Freudenberg KG | Tissu composite non tissé |
| PL4506155T3 (pl) | 2023-08-07 | 2026-04-20 | Carl Freudenberg Kg | Włóknina kompozytowa |
| PL4506153T3 (pl) | 2023-08-07 | 2026-04-13 | Carl Freudenberg Kg | Zastosowanie materiału włókienniczego jako geowłókniny kapilarnej |
| CN121969495A (zh) | 2023-08-07 | 2026-05-01 | 科德宝两合公司 | 非织造复合织物 |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3531368A (en) * | 1966-01-07 | 1970-09-29 | Toray Industries | Synthetic filaments and the like |
| US4239720A (en) * | 1978-03-03 | 1980-12-16 | Akzona Incorporated | Fiber structures of split multicomponent fibers and process therefor |
| DE2907623A1 (de) * | 1979-02-27 | 1980-09-04 | Akzo Gmbh | Verfahren zur herstellung von fibrillierten faserstrukturen |
| FR2546536B1 (fr) * | 1983-05-25 | 1985-08-16 | Rhone Poulenc Fibres | Procede pour le traitement de nappes non tissees et produit obtenu |
| FR2657893B1 (fr) * | 1990-02-08 | 1993-04-02 | Rhone Poulenc Fibres | Nontisses de filaments continus synthetiques dont au moins une partie a proprietes de surface modifiees, procede pour leur fabrication et leurs applications. |
| US5047189A (en) * | 1990-05-11 | 1991-09-10 | Nan Ya Plastics Corporation | Process for preparing partially dissolvable and splittable conjugated microfiber |
| JP3070632B2 (ja) * | 1991-11-21 | 2000-07-31 | ユニチカ株式会社 | 柔軟性不織布及びその製造方法 |
| JP3102450B2 (ja) * | 1992-10-05 | 2000-10-23 | ユニチカ株式会社 | 三層構造不織布及びその製造方法 |
| JP3113124B2 (ja) * | 1993-07-02 | 2000-11-27 | 帝人株式会社 | 極細繊維ウエブの製造方法 |
-
1996
- 1996-06-17 FR FR9607659A patent/FR2749860B1/fr not_active Expired - Lifetime
-
1997
- 1997-05-23 DE DE69725051T patent/DE69725051T2/de not_active Expired - Lifetime
- 1997-05-23 EP EP97108364A patent/EP0814188B1/fr not_active Expired - Lifetime
- 1997-06-05 CA CA002208117A patent/CA2208117C/fr not_active Expired - Lifetime
- 1997-06-12 ZA ZA9705216A patent/ZA975216B/xx unknown
- 1997-06-16 JP JP9159002A patent/JPH1053948A/ja active Pending
- 1997-06-16 CN CN97112798A patent/CN1093191C/zh not_active Expired - Lifetime
- 1997-06-17 BR BR9703602A patent/BR9703602A/pt not_active IP Right Cessation
- 1997-06-17 US US08/877,111 patent/US5899785A/en not_active Expired - Lifetime
- 1997-07-09 TW TW086109666A patent/TW348192B/zh not_active IP Right Cessation
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102004036099A1 (de) * | 2004-07-24 | 2006-03-16 | Carl Freudenberg Kg | Mehrpomponenten-Spinnvliesstoff, Verfahren zu seiner Herstellung sowie Verwendung der Mehrkomponenten-Spinnvliesstoffe |
| DE102004036099B4 (de) * | 2004-07-24 | 2008-03-27 | Carl Freudenberg Kg | Mehrkomponenten-Spinnvliesstoff, Verfahren zu seiner Herstellung sowie Verwendung der Mehrkomponenten-Spinnvliesstoffe |
| EP1891871A2 (fr) | 2006-08-26 | 2008-02-27 | Bleuel, Norbert | Dispositif de polissage, de nettoyage ou de séchage de l'intérieur d'un récipient pour recevoir des liquides |
| EP1891871B1 (fr) * | 2006-08-26 | 2012-04-25 | Bleuel, Norbert | Dispositif de polissage, de nettoyage ou de séchage de l'intérieur d'un récipient pour recevoir des liquides |
| DE102007041630A1 (de) | 2007-09-03 | 2009-03-05 | Carl Freudenberg Kg | Verfahren zur Herstellung eines Flächengebildes aus zumindest teilweise gesplitteten Garnen, Fasern oder Filamenten und Vorrichtung zu dessen Herstellung |
| DE102007041630B4 (de) * | 2007-09-03 | 2010-09-30 | Carl Freudenberg Kg | Verfahren zur Herstellung eines Flächengebildes aus zumindest teilweise gesplitteten Garnen, Fasern oder Filamenten und Vorrichtung zu dessen Herstellung |
| WO2012155980A1 (fr) * | 2011-05-19 | 2012-11-22 | Gardena Manufacturing Gmbh | Conduite d'eau pour système d'arrosage de plantes et système d'arrosage de plantes |
Also Published As
| Publication number | Publication date |
|---|---|
| BR9703602A (pt) | 1998-11-10 |
| CA2208117A1 (fr) | 1997-12-17 |
| DE69725051T2 (de) | 2004-07-15 |
| US5899785A (en) | 1999-05-04 |
| FR2749860A1 (fr) | 1997-12-19 |
| ZA975216B (en) | 1998-01-05 |
| JPH1053948A (ja) | 1998-02-24 |
| FR2749860B1 (fr) | 1998-08-28 |
| EP0814188A1 (fr) | 1997-12-29 |
| DE69725051D1 (de) | 2003-10-30 |
| CN1171463A (zh) | 1998-01-28 |
| CN1093191C (zh) | 2002-10-23 |
| CA2208117C (fr) | 2001-01-16 |
| TW348192B (en) | 1998-12-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0814188A1 (fr) | Nappe nontissée formée de filaments continus très fins | |
| US5970583A (en) | Nonwoven lap formed of very fine continuous filaments | |
| EP0694644B1 (fr) | Procédé de fabrication d'une nappe de non-tissé constituée de filaments continus liés entre eux et nappe ainsi obtenue | |
| EP0648878B1 (fr) | Entoilage thermocollant comportant une nappe de fibres entremêlées dans des fils de trame texturés et son procédé de fabrication | |
| US6460233B2 (en) | Process for the production of a complex nonwoven material and novel type of material thus obtained | |
| CA2154669C (fr) | Procede de fabrication d'un non-tisse et non-tisse obtenu par ce procede | |
| EP0390622B1 (fr) | Textile destiné à l'entoilage et son procédé de fabrication | |
| JP6422988B2 (ja) | マイクロファイバー不織布複合物 | |
| CA1226426A (fr) | Procede pour le traitement de nappes non-tissees et produit obtenu | |
| FR2794776A1 (fr) | Procede pour la realisation d'un materiau non tisse, installation pour sa mise en oeuvre et non tisse ainsi obtenu | |
| JP2002534616A (ja) | 三次元構造化された繊維平面形成物およびその製造方法 | |
| MXPA04010108A (es) | Laminado de fibra y metodo para producir un laminado de fibra. | |
| FR2803604A1 (fr) | Procede pour la realisation d'un materiau non tisse complexe et nouveau type de materiau ainsi obtenu | |
| JP6692750B2 (ja) | クリーニングクロス | |
| CN101641469B (zh) | 由原纤化双组分海岛纤维生产的高强耐用微米和纳米纤维织物 | |
| FR2790489A1 (fr) | Nappe non tissee en filaments ou fibres thermolie(e)s | |
| EP0501842B1 (fr) | Textile d'entoilage composite | |
| TWI633219B (zh) | 用於製造結構化的微絲非織造物的方法 | |
| JP5902257B2 (ja) | 複合不織シートの製造方法 | |
| FR2458618A1 (fr) | Procede pour la fabrication de produits en nappe de fibres non tisses avec pouvoir de retour dans la forme | |
| EP4592072B1 (fr) | Tissu composite non tissé | |
| JP7671146B2 (ja) | 意匠シート及びその製造方法 | |
| JP7298880B2 (ja) | 毛羽立ちの少ない柄付き不織布の製造方法 | |
| FR2664623A1 (fr) | Entoilage thermocollant a base de microfibres et procede pour l'obtenir. | |
| WO2025031744A1 (fr) | Tissu composite non tissé |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE ES FR GB IT NL |
|
| 17P | Request for examination filed |
Effective date: 19980604 |
|
| 17Q | First examination report despatched |
Effective date: 20000911 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: CARL FREUDENBERG KG |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB IT NL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030924 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20030924 Ref country code: GB Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030924 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030924 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REF | Corresponds to: |
Ref document number: 69725051 Country of ref document: DE Date of ref document: 20031030 Kind code of ref document: P |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| GBV | Gb: ep patent (uk) treated as always having been void in accordance with gb section 77(7)/1977 [no translation filed] |
Effective date: 20030924 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20040625 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20160531 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20160512 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 69725051 Country of ref document: DE |