EP1842640A2 - Vibrating table for vibrating presses - Google Patents
Vibrating table for vibrating presses Download PDFInfo
- Publication number
- EP1842640A2 EP1842640A2 EP07105447A EP07105447A EP1842640A2 EP 1842640 A2 EP1842640 A2 EP 1842640A2 EP 07105447 A EP07105447 A EP 07105447A EP 07105447 A EP07105447 A EP 07105447A EP 1842640 A2 EP1842640 A2 EP 1842640A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- shafts
- vibrating
- motors
- motor
- type
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B1/00—Producing shaped prefabricated articles from the material
- B28B1/08—Producing shaped prefabricated articles from the material by vibrating or jolting
- B28B1/087—Producing shaped prefabricated articles from the material by vibrating or jolting by means acting on the mould ; Fixation thereof to the mould
- B28B1/0873—Producing shaped prefabricated articles from the material by vibrating or jolting by means acting on the mould ; Fixation thereof to the mould the mould being placed on vibrating or jolting supports, e.g. moulding tables
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B06—GENERATING OR TRANSMITTING MECHANICAL VIBRATIONS IN GENERAL
- B06B—METHODS OR APPARATUS FOR GENERATING OR TRANSMITTING MECHANICAL VIBRATIONS OF INFRASONIC, SONIC, OR ULTRASONIC FREQUENCY, e.g. FOR PERFORMING MECHANICAL WORK IN GENERAL
- B06B1/00—Methods or apparatus for generating mechanical vibrations of infrasonic, sonic, or ultrasonic frequency
- B06B1/10—Methods or apparatus for generating mechanical vibrations of infrasonic, sonic, or ultrasonic frequency making use of mechanical energy
- B06B1/16—Methods or apparatus for generating mechanical vibrations of infrasonic, sonic, or ultrasonic frequency making use of mechanical energy operating with systems involving rotary unbalanced masses
- B06B1/161—Adjustable systems, i.e. where amplitude or direction of frequency of vibration can be varied
- B06B1/166—Where the phase-angle of masses mounted on counter-rotating shafts can be varied, e.g. variation of the vibration phase
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B3/00—Producing shaped articles from the material by using presses; Presses specially adapted therefor
- B28B3/02—Producing shaped articles from the material by using presses; Presses specially adapted therefor wherein a ram exerts pressure on the material in a moulding space; Ram heads of special form
- B28B3/022—Producing shaped articles from the material by using presses; Presses specially adapted therefor wherein a ram exerts pressure on the material in a moulding space; Ram heads of special form combined with vibrating or jolting
Definitions
- the present invention relates to the field of apparatuses for the production of prefabricated construction elements and specifically to the field of vibrating presses for the moulding of concrete artefacts.
- the moulding process generally comprises the filling of specific moulds with a viscous granular mixture of the material to be employed, the levelling of said viscous material - for example, by means of appropriate filling and shaking means so as to apply considerable vibratory forces to said moulds - and the subsequent application to said moulds of a considerable pressure, induced by specific vibrators, so as to expel the water present in the viscous mixture and promote the compacting thereof.
- the aforesaid moulding process is generally performed by means of vibrating presses which are provided with a horizontal table induced to vibrate by appropriate vertical action vibrating means.
- the moulds for making concrete artefacts are placed on said horizontal table.
- Said moulds are filled with the viscous pre-mixed concrete mixture - or similar construction material - by appropriate dispensers during their movement on the horizontal table of said press.
- the filling of these moulds occurs with a decreasing amount of material as the distance of the shapes of the products obtained in the moulds from said dispensers increases, the vibratory motion to which the moulds are subjected by the horizontal table on which they are placed, favours and makes easy the distribution of the viscous construction material within the moulds themselves, thus overcoming the disuniformity induced by the described nonhomogeneous filling.
- the solution of subdividing the horizontal vibrating table into two independent halves subjected to two vibrations modulated in different manner is often adopted.
- the present invention relates to a vibrating table for vibrating presses used in the moulding of concrete artefacts.
- Said vibrating table comprising an appropriate actuating and control system, is adapted to make the mould filling operations with mixtures for the preparation of construction materials, and of concrete in particular, more effective.
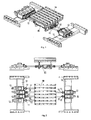
- Fig. 1 shows in detail the vibrating table for vibrating presses for the production of construction materials, such as concrete and the like, according to the present invention.
- It comprises a single vibrating table 10 associated to a plurality of eccentric shafts 15 in turn associated, by means of appropriate connection means 11, to drive shafts 12 each connected, in turn, to a motor 13 fixed to appropriate supporting means 14.
- Said motors 13 are in turn controlled so as to modulate and vary the type of vibration to which said vibrating table 10 is subjected, thus adapting the operating mode of the apparatus according to the present invention to the needs of the material to be employed and the type of artefacts to be manufactured.
- said eccentric shafts 15 are six in number.
- Each of said eccentric shafts 15 is connected to a motor 13 by means of said drive shafts 12, the motor is electric, preferably of the type controlled by inverter and having the rotation speed regulated by an appropriate electronic control module, preferably associated to an encoder device for reading the number of rounds per minute and the instantaneous angular position of the shaft of said motor (13).
- Said electronic control module allows the operator to set the revolution speed of each shaft in terms of angular speed of the axis and reciprocal angular offset between one shaft and the other. In this manner, it is possible, by composing the centrifuge forces developed by each shaft, to obtain a component of the resulting force applied to said vibrating table having vertical direction, alternating sign direction and adjustable intensity, so as to develop the desired unidirectional vibratory effect in the desired part of said vibrating table.
- drive shafts 12 associated to said vibrating table are arranged as shown in Fig. 2.
- Four drive shafts 12 on the first side of the vibrating table are such that the two central shafts have a shorter length with respect to the two peripheral shafts, while the two shafts on the second side of said vibrating table are arranged in the two central positions and have the same length as the two central shafts on the first side of the vibrating table. In this manner, the vibrating table will be subjected to a higher resulting vertical force in one half of the table with respect to the other half.
- the structure of said vibrating table 10 is made of construction steel plates, but other materials having similar features of robustness and machineability may be employed.
- Eccentric shafts 15 must be characterised by suitable strength and robustness and may be made of special steel, e.g. starting from a laminate of the commercial type, which is milled, turned, refaced and has been locally thermally treated where required. Said eccentric shafts 15 are preferably supported by bearings accommodated within appropriately lubricated fluid-tight supports.
- Connection means 11, associated to said Cardan drive shafts 12, may preferably consist of appropriate universal joints.
- Said Cardan drive shafts 12, in turn, may be of the tubular type, adapted for high rotation speeds, and dynamically balanced.
- Supporting means 14 comprise welded mechanical structures adapted to support the electric motors and perform the structural connection with the main structure of the vibrating press according to the present invention.
- employed electric motors 13 are preferably of the asynchronous lamellar type of high specific power provided with a servo ventilation system. They are further provided with a contactless rotary inverter for detecting the rotation speed and the instantaneous angular position of the motor axis. Said electric motors 13 are preferably driven by appropriate inverters, e.g. of the vectorial type, adapted to ensure the regulation in accordance with the various required operating speeds by varying the supply current frequency of the motors themselves.
- An appropriate programmable controller provided with a specific control software will control said inverter so as to define the operating profiles of the entire system, by means of the management of parameters which are adjustable by the system user, such as for example:
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Chemical & Material Sciences (AREA)
- Ceramic Engineering (AREA)
- Apparatuses For Generation Of Mechanical Vibrations (AREA)
- Devices For Post-Treatments, Processing, Supply, Discharge, And Other Processes (AREA)
- Press-Shaping Or Shaping Using Conveyers (AREA)
Abstract
Description
- The present invention relates to the field of apparatuses for the production of prefabricated construction elements and specifically to the field of vibrating presses for the moulding of concrete artefacts.
- In the field of the production of concrete artefacts, the most used technique is that comprising moulding by means of vibrating presses.
- The moulding process generally comprises the filling of specific moulds with a viscous granular mixture of the material to be employed, the levelling of said viscous material - for example, by means of appropriate filling and shaking means so as to apply considerable vibratory forces to said moulds - and the subsequent application to said moulds of a considerable pressure, induced by specific vibrators, so as to expel the water present in the viscous mixture and promote the compacting thereof. The aforesaid moulding process is generally performed by means of vibrating presses which are provided with a horizontal table induced to vibrate by appropriate vertical action vibrating means. The moulds for making concrete artefacts are placed on said horizontal table. Said moulds are filled with the viscous pre-mixed concrete mixture - or similar construction material - by appropriate dispensers during their movement on the horizontal table of said press. The filling of these moulds occurs with a decreasing amount of material as the distance of the shapes of the products obtained in the moulds from said dispensers increases, the vibratory motion to which the moulds are subjected by the horizontal table on which they are placed, favours and makes easy the distribution of the viscous construction material within the moulds themselves, thus overcoming the disuniformity induced by the described nonhomogeneous filling. In order to further improve the homogeneous filling of the moulds, the solution of subdividing the horizontal vibrating table into two independent halves subjected to two vibrations modulated in different manner is often adopted. In this manner, by regulating the amplitude, the frequency and the duration of the vibration of the half table farthest from the dispenser to higher values with respect to regulating values of the closest half table, the filling of the mould and thus the volume mass of the compacted products resulting from the process may be levelled more precisely.
- This solution, along with others belonging to the state of the art, however displays the drawback of requiring electronic circuits and complex mechanical constructions which have repercussions on the easiness of use and on the cost of the final apparatus.
- The present invention relates to a vibrating table for vibrating presses used in the moulding of concrete artefacts. Said vibrating table, comprising an appropriate actuating and control system, is adapted to make the mould filling operations with mixtures for the preparation of construction materials, and of concrete in particular, more effective.
-
- Fig. 1 Axonometric view of the vibrating table for vibrating presses according to the present invention.
- Fig. 2 Plan and perspective view of a preferred embodiment of the vibrating table for vibrating presses according to the present invention.
- Fig. 1 shows in detail the vibrating table for vibrating presses for the production of construction materials, such as concrete and the like, according to the present invention.
- It comprises a single vibrating table 10 associated to a plurality of
eccentric shafts 15 in turn associated, by means of appropriate connection means 11, to driveshafts 12 each connected, in turn, to amotor 13 fixed toappropriate supporting means 14. - Said
motors 13 are in turn controlled so as to modulate and vary the type of vibration to which said vibrating table 10 is subjected, thus adapting the operating mode of the apparatus according to the present invention to the needs of the material to be employed and the type of artefacts to be manufactured. - In a preferred embodiment of the apparatus according to the present invention, said
eccentric shafts 15 are six in number. Each of saideccentric shafts 15 is connected to amotor 13 by means of saiddrive shafts 12, the motor is electric, preferably of the type controlled by inverter and having the rotation speed regulated by an appropriate electronic control module, preferably associated to an encoder device for reading the number of rounds per minute and the instantaneous angular position of the shaft of said motor (13). - Said electronic control module allows the operator to set the revolution speed of each shaft in terms of angular speed of the axis and reciprocal angular offset between one shaft and the other. In this manner, it is possible, by composing the centrifuge forces developed by each shaft, to obtain a component of the resulting force applied to said vibrating table having vertical direction, alternating sign direction and adjustable intensity, so as to develop the desired unidirectional vibratory effect in the desired part of said vibrating table.
- In the mentioned preferred embodiment of the apparatus according to the present invention, drive
shafts 12 associated to said vibrating table are arranged as shown in Fig. 2. Fourdrive shafts 12 on the first side of the vibrating table are such that the two central shafts have a shorter length with respect to the two peripheral shafts, while the two shafts on the second side of said vibrating table are arranged in the two central positions and have the same length as the two central shafts on the first side of the vibrating table. In this manner, the vibrating table will be subjected to a higher resulting vertical force in one half of the table with respect to the other half. Therefore, while maintaining the position of the dispenser centred and symmetric during the filling of the mould, as an effect, the filling of the mould itself will be facilitated as the distance of the dispenser increases and, therefore, the amount of viscous construction material, e.g. "soft" concrete, which enters said moulds, may be levelled. - Preferably, the structure of said vibrating table 10 is made of construction steel plates, but other materials having similar features of robustness and machineability may be employed.
-
Eccentric shafts 15 must be characterised by suitable strength and robustness and may be made of special steel, e.g. starting from a laminate of the commercial type, which is milled, turned, refaced and has been locally thermally treated where required. Saideccentric shafts 15 are preferably supported by bearings accommodated within appropriately lubricated fluid-tight supports. - Connection means 11, associated to said Cardan
drive shafts 12, may preferably consist of appropriate universal joints. Said Cardan driveshafts 12, in turn, may be of the tubular type, adapted for high rotation speeds, and dynamically balanced. - Supporting means 14 comprise welded mechanical structures adapted to support the electric motors and perform the structural connection with the main structure of the vibrating press according to the present invention.
- Regarding employed
electric motors 13, these are preferably of the asynchronous lamellar type of high specific power provided with a servo ventilation system. They are further provided with a contactless rotary inverter for detecting the rotation speed and the instantaneous angular position of the motor axis. Saidelectric motors 13 are preferably driven by appropriate inverters, e.g. of the vectorial type, adapted to ensure the regulation in accordance with the various required operating speeds by varying the supply current frequency of the motors themselves. - An appropriate programmable controller provided with a specific control software will control said inverter so as to define the operating profiles of the entire system, by means of the management of parameters which are adjustable by the system user, such as for example:
- contemporaneity or consequentiality of the steps.
- Electric motor rotation speed.
- Relative angular positions of the motor axes and thus of the motor axis-drive shaft-eccentric shaft kinematic chain and their progress in time.
- Accelerations and decelerations of the single shafts.
Claims (17)
- A vibrating supporting device for vibrating presses comprising a metal table (10) associated to a plurality of eccentric shafts (15) in turn associated, by means of appropriate connection means (11) to a plurality of drive shafts (12) each connected in turn to a motor (13) anchored to appropriate supporting means (14).
- A device according to claim 1, characterised in that said motors (13) are of the electrical type.
- A device according to claims 1-2, characterised in that said motors (13) are driven by driving inverters.
- A device according to claim 3, characterised in that said driving inverters of said motors (13) are associated to at least one electronic control module adapted to regulate the rotation speed in terms of angular speed of the axis of each motor (13) and reciprocal angular offset between shafts of different motors.
- A device according to claim 4, characterised in that said at least one electronic control device is associated to an encoder type device for reading the number of rounds per minute and the instantaneous angular position of the shaft of said motor (13).
- A device according to claims 4-5, characterised in that said electronic control module regulates the parameters related to said motor (13) selected from the group comprising: contemporaneity or consequentiality of the steps; rotation speed of said electric motors (13); relative angular positions of the motor axes and thus of the motor (13) axis - drive shaft (12) - eccentric shaft (15) kinematic chain and their progress in time; accelerations and decelerations of the single shafts of said motors (13).
- A device according to claims 2-6, characterised in that said electric motors (13) are of the of the asynchronous lamellar type of high specific power and are provided with a servo ventilation system.
- A device according to claims 1-7, characterised in that said drive shafts (12) associated to said metal table (10) are six in number, four of which are arranged on a first side of said metal table (10) and two of which are arranged on the side opposite to said first side.
- A device according to claim 8, characterised in that said four drive shafts (12) arranged on one first side of said metal table (10) are such that the two central shafts have a shorter length with respect to the two peripheral shafts, while said two shafts arranged on the side opposite to said first side are arranged in the two central positions and have the same length as the two central shafts on said first side of said metal table (10).
- A device according to claims 1-9, characterised in that said vibrating table (10) is made of construction steel plates.
- A device according to claims 1-10, characterised in that said eccentric shafts (15) are formed of special steel of the commercial type, which is machined and thermally treated.
- A device according to claims 1-11, characterised in that said eccentric shafts (15) are supported by bearings accommodated in appropriately lubricated fluid-tight supports.
- A device according to claims 1-12, characterised in that said drive shafts (12) are of the Cardan type.
- A device according to claims 1-13 characterised in that said connection means (11), associated to said drive shafts (12) are made by appropriate universal joints.
- A device according to claims 1-14, characterised in that said drive shafts (12) are of the tubular and dynamically balanced type.
- A device according to claims 1-15, characterised in that said supporting means (14) comprise welded mechanical structures adapted to support said motors (13) and perform the structural connection with the main structure of the vibrating press.
- A vibrating press for the production of construction materials characterised in that it comprises a vibrating supporting device according to claims 1-16.
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| ITFI20060088 ITFI20060088A1 (en) | 2006-04-03 | 2006-04-03 | VIBRATING FLOOR FOR VIBROPRESSE |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1842640A2 true EP1842640A2 (en) | 2007-10-10 |
| EP1842640A3 EP1842640A3 (en) | 2010-09-29 |
| EP1842640B1 EP1842640B1 (en) | 2012-08-15 |
Family
ID=38235192
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP20070105447 Active EP1842640B1 (en) | 2006-04-03 | 2007-04-02 | Vibrating table for vibrating presses |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP1842640B1 (en) |
| ES (1) | ES2392660T3 (en) |
| IT (1) | ITFI20060088A1 (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2147779A1 (en) * | 2008-07-25 | 2010-01-27 | Quadra 1 | Vibrating press for the production of construction elements and method for producing construction elements |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN105856384A (en) * | 2016-05-20 | 2016-08-17 | 黑龙江省中信路桥材料有限公司 | Vibrating platform applicable to dry concrete product production |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4116647C5 (en) * | 1991-05-22 | 2004-07-08 | Hess Maschinenfabrik Gmbh & Co. Kg | shaker |
| DE29712242U1 (en) * | 1997-07-11 | 1997-09-18 | Lonz Industrieautomation GmbH, 65510 Hünstetten | Unbalance shaker |
| DE19812986C1 (en) * | 1998-03-24 | 1999-11-11 | Masa Ag | Unbalance shaker for stone molding machines |
| DE20301954U1 (en) * | 2003-02-05 | 2003-04-24 | Institut für Fertigteiltechnik und Fertigbau Weimar e.V., 99423 Weimar | Device for shaping batches |
-
2006
- 2006-04-03 IT ITFI20060088 patent/ITFI20060088A1/en unknown
-
2007
- 2007-04-02 EP EP20070105447 patent/EP1842640B1/en active Active
- 2007-04-02 ES ES07105447T patent/ES2392660T3/en active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2147779A1 (en) * | 2008-07-25 | 2010-01-27 | Quadra 1 | Vibrating press for the production of construction elements and method for producing construction elements |
Also Published As
| Publication number | Publication date |
|---|---|
| ES2392660T3 (en) | 2012-12-12 |
| ITFI20060088A1 (en) | 2007-10-04 |
| EP1842640B1 (en) | 2012-08-15 |
| EP1842640A3 (en) | 2010-09-29 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| KR101858523B1 (en) | Press for vacuum vibro-compression of slabs or blocks or articles of agglomerated or ceramic materila | |
| CA2087849C (en) | Vibrator | |
| US7527487B2 (en) | Device for moulding mixtures | |
| US20040051197A1 (en) | Compaction device for compacting moulded bodies from granular substances and method for using said device | |
| RU2645025C2 (en) | Method of casting concrete products and corresponding apparatus | |
| EP1842640B1 (en) | Vibrating table for vibrating presses | |
| RU2168412C2 (en) | Roll-type smoothing machine with smoothing device vibrating in transverse direction | |
| US20140283633A1 (en) | Vibration exciter, in particular for a construction machine | |
| EP0359572B1 (en) | Method and slide-casting machine for casting of one or several concrete products placed side by side | |
| CN103909560B (en) | A kind of automatic frequency-conversion luffing vibrating device and vibration control method thereof | |
| CN109047689A (en) | Single servo motor two-side synchronous drives mould non-sinusoidal vibration device | |
| CN201165025Y (en) | Novel vibration device of block-making machine | |
| EP0945188A3 (en) | Unbalanced-mass vibrator for a beton moulding machine | |
| US5983752A (en) | Adjustable counterweight system for a machine for forming concrete blocks, pavers or the like | |
| KR20140043093A (en) | Surface compactor and method of operation | |
| US1968711A (en) | Method and apparatus for vibrating | |
| CN101229652A (en) | Novel type block machine vibrator | |
| KR100540755B1 (en) | Liquid filling amount control device of soft gelatin capsule maker | |
| CN2858227Y (en) | Vibration device for building-block machine | |
| KR101971213B1 (en) | The Device of Forming Flat-Cured Film | |
| CN219705561U (en) | Vibration system of block forming machine | |
| RU2130379C1 (en) | Disc-type smoothing machine with vibrating operating member | |
| ES2206484T3 (en) | A BLOCK MANUFACTURING MACHINE. | |
| RU2036083C1 (en) | Table vibrator for moulding of reinforced-concrete products | |
| CN117734004B (en) | Cement pole pouring rapid prototyping equipment |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK YU |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: FORM IMPIANTI S.P.A. |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR MK RS |
|
| 17P | Request for examination filed |
Effective date: 20110329 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| 17Q | First examination report despatched |
Effective date: 20110727 |
|
| GRAJ | Information related to disapproval of communication of intention to grant by the applicant or resumption of examination proceedings by the epo deleted |
Free format text: ORIGINAL CODE: EPIDOSDIGR1 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC MT NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Ref country code: CH Ref legal event code: EP Ref country code: AT Ref legal event code: REF Ref document number: 570569 Country of ref document: AT Kind code of ref document: T Effective date: 20120815 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602007024714 Country of ref document: DE Effective date: 20121011 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2392660 Country of ref document: ES Kind code of ref document: T3 Effective date: 20121212 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20120815 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20121215 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20121116 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20121217 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20130516 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20121115 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602007024714 Country of ref document: DE Effective date: 20130516 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20130402 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130430 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130402 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130402 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 570569 Country of ref document: AT Kind code of ref document: T Effective date: 20130402 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130402 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120815 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20070402 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130402 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 12 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230613 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250408 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20250506 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20250424 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20250409 Year of fee payment: 19 |