WO2005001149A2 - Produits en alliages al-zn-mg-cu a compromis caracteristiques mecaniques statiques/tolerance aux dommages ameliore - Google Patents
Produits en alliages al-zn-mg-cu a compromis caracteristiques mecaniques statiques/tolerance aux dommages ameliore Download PDFInfo
- Publication number
- WO2005001149A2 WO2005001149A2 PCT/FR2004/001571 FR2004001571W WO2005001149A2 WO 2005001149 A2 WO2005001149 A2 WO 2005001149A2 FR 2004001571 W FR2004001571 W FR 2004001571W WO 2005001149 A2 WO2005001149 A2 WO 2005001149A2
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- mpa
- mpavm
- product according
- hours
- temperature
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C21/00—Alloys based on aluminium
- C22C21/10—Alloys based on aluminium with zinc as the next major constituent
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22F—CHANGING THE PHYSICAL STRUCTURE OF NON-FERROUS METALS AND NON-FERROUS ALLOYS
- C22F1/00—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working
- C22F1/04—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working of aluminium or alloys based thereon
- C22F1/053—Changing the physical structure of non-ferrous metals or alloys by heat treatment or by hot or cold working of aluminium or alloys based thereon of alloys with zinc as the next major constituent
Definitions
- the present invention relates to alloys of the Al-Zn-Mg-Cu type with compromise static mechanical characteristics - improved damage tolerance, as well as structural elements for aeronautical construction incorporating wrought semi-finished products produced from these alloys.
- Alloys of the Al-Zn-Mg-Cu type (belonging to the family of 7xxx alloys) are commonly used in aeronautical construction, and in particular in the construction of the wings of civil aircraft.
- the alloys 7150, 7050 and 7349 are also used for the manufacture of fuselage stiffeners.
- the 7475 alloy is sometimes used for the manufacture of lower airfoil panels, in particular by machining heavy sheets, while the lower airfoil stiffeners are usually made of 2xxx type alloys (eg 2024, 2224, 2027).
- alloys 7075 and 7175 (zinc content between 5.1 and 6.1% by weight), 7475 (zinc content between 5.2 and 6.2%) , 7050 (zinc content between 5.7 and 6.7%), 7150 (zinc content between 5.9 and 6.9%) and 7049 (zinc content between 7.2 and 8.2%). These alloys have different compromises between toughness and elastic limit.
- Patent application EP 0 257 167 A1 describes an alloy developed specifically for the production by reverse spinning of pressure-resistant hollow bodies. This alloy has the composition (in percent by mass): Zn 6.25 - 8.0 Mg 1.2 - 2.2 Cu 1.7 - 2.8 Zr ⁇ 0.05 Fe ⁇ 0.20 (Fe + Si) ⁇ 0.40 Cr 0.15 - 0.28 Mn ⁇ 0.20 Ti ⁇ 0.05.
- US Patent 5,865,911 (Aluminum Company of America) discloses an Al-Zn-Cu-Mg type alloy of composition Zn 5.9 -6.7, Mg 1.6- 1.86, Cu 1.8 -2.4 , Zr 0.08-0.15 for the manufacture of structural elements for aircraft. These structural elements are optimized to show strong mechanical strength, toughness and resistance to fatigue.
- Patent application WO 02/052053 describes three alloys of the Al-Zn-Cu-Mg type with the composition Zn7.3 Cul, 6, Zn6.7 Cu 1.9, Zn7.4 Cul, 9 and each comprising Mg 1.5 Zr 0.11, as well as thermomechanical treatment methods suitable for the manufacture of structural elements for aircraft.
- Alloy 7040 is also known, the standardized chemical composition of which is: Zn 5.7 -6.7 Mg 1.7-2.4 Cu 1.5 -2.3 Zr 0.05 -0.12 Si ⁇ 0 , 10 Fe ⁇ 0.13 Ti ⁇ 0.06 Mn ⁇ 0.04 other elements ⁇ 0.05 each and ⁇ 0.15 in total.
- Alloy 7085 is also known, the standardized chemical composition of which is: Zn 7.0 -8.0 Mg 1.2 -1.8 Cu 1.3 -2.0 Zr 0.08 -0.15 If ⁇ 0, 06 Fe ⁇ 0.08 Ti ⁇ 0.06 Mn ⁇ 0.04 Cr ⁇ 0.04 other elements ⁇ 0.05 each and ⁇ 0.15 in total.
- the problem to which the present invention is trying to respond is to propose a new wrought product of Al-Zn-Mg-Cu type alloy making it possible to achieve very high levels of static mechanical strength while presenting a level sufficient in other properties of use, in particular the toughness, the resistance to corrosion and the resistance to the propagation of fatigue cracks (cracking).
- a first object of the present invention consists of a spun, rolled or forged product made of aluminum alloy, characterized in that it comprises (in% by mass): Zn 6.7 - 7.5% Cu 2.0 - 2.8% Mg 1.6 - 2.2% one or more elements chosen from the group consisting of: Zr 0.08 - 0.20% Cr 0.05 - 0.25% Se 0.01 - 0.50 % Hf 0.05 - 0.20% N 0.02 - 0.20% Fe + Si ⁇ 0.20% other elements ⁇ 0.05% each and ⁇ 0.15% in total, the rest aluminum.
- Another object of the present invention is a manufacturing process for obtaining such a product.
- Yet another object of the present invention is an aircraft structural element which incorporates at least one of said products, and in particular a structural element used in the construction of the wing of civil aircraft, such as a stiffener, and in in particular a wing lower stiffener.
- FIG. 1 shows the section of "I” profiles, the manufacture of which is described in Example 1.
- 1 thick branch
- 2 Thickness of the thick branch
- 3 sole
- 4 thickness of the sole 3
- 5 long branch
- 6 height
- 7 width
- FIG. 2 shows the section of profiles whose manufacture is described in Examples 3 and 5.
- the metallurgical states are defined in European standard EN 515.
- the chemical composition of standardized aluminum alloys is defined for example in standard EN 573-3.
- the static mechanical characteristics that is to say the tensile strength R m , the elastic limit Rpo. 2 , and the elongation at break A, are determined by a tensile test according to standard EN 10002-1, the place and direction of the sampling of the test pieces being defined in standard EN 485-1.
- the elastic limit in compression was measured by a test according to ASTM E9.
- the tenacity Kic was measured according to standard ASTM E 399.
- the curve R is determined according to standard ASTM 561-98.
- machining includes any material removal process such as turning, milling, drilling, reaming, tapping, EDM, grinding, polishing.
- spun product also includes products which have been drawn after spinning, for example by cold drawing through a die. It also includes drawn products.
- structural element refers to an element used in mechanical construction for which the static and / or dynamic mechanical characteristics are of particular importance for the performance and integrity of the structure, and for which a calculation of the structure is generally prescribed or performed. It is typically a mechanical part, the failure of which is likely to endanger the safety of said construction, of its users, of its users or of others.
- these structural elements include in particular the elements that make up the fuselage (such as the fuselage skin), the stiffeners or bulkheads, bulkheads, fuselage (circumferential frames), the wings (such as the wing skin), the stiffeners (stringers or stiffeners), the ribs (ribs) and spars (spars)) and the empennage composed in particular of horizontal and vertical stabilizers (horizontal or vertical stabilizers), as well as the floor profiles (floor beams), the seat rails (seat tracks) and the doors.
- monolithic structural element refers to a structural element which has been obtained from a single piece of rolled, spun, forged or molded semi-finished product, without assembly, such as riveting, welding, bonding, with another room.
- TEQ 160 ° C
- Q an activation energy of 132000 kj / mol
- R 8.31 kJ / mol / (° K).
- the problem is solved by the combination of a fine adjustment of the content of alloying elements and of the conditions of the heat treatment, in particular of the homogenization of the raw forms, as well as the dissolution and the income of the products obtained by hot transformation.
- an alloy of composition Zn 6.7 - 7.5 (preferably: 6.9 - 7.3) is first prepared; Cu 2.0 - 2.8 (preferably 2.2 - 2.6); Mg 1.6-2.2 (preferably 1.8-2.0); one or more elements chosen from the group consisting of Zr 0.08 - 0.20, Cr 0.05 - 0.40, Se 0.01 - 0.50, Hf 0.05 - 0.60, N 0.02 - 0.20; Fe + Si ⁇ 0.20 and preferably ⁇ 0.15; other items ⁇ 0.05 each and ⁇ 0.15 in total; the rest aluminum.
- the content of alloying elements must not significantly exceed their solubility limit, because otherwise, the persistence of intermetallic phases during dissolution which can harm tolerance for damage.
- the copper content can be brought to a level fairly close to the solubility limit, which depends on the magnesium content.
- a composition is preferred in which 3.8 ⁇ Cu + Mg ⁇ 4.8, and preferably 3.9 ⁇ Cu + Mg ⁇ 4.7.
- 4.0 ⁇ Cu + Mg ⁇ 4.8 is chosen.
- 4.1 ⁇ Cu + Mg ⁇ 4.7 is chosen.
- the Cu / Mg ratio must be at least 1.0 in order to obtain a good compromise of properties, and in particular a good tolerance for damage, but must not exceed 1.5 to ensure acceptable flowability. It is preferred that it be between 1.1 and 1.5, and even more preferably between 1.1 and 1.4. The Applicant has found that above a magnesium content of approximately 2.2%, we no longer obtain acceptable tenacity properties.
- the magnesium and copper content is chosen such that 4.2 ⁇ Cu + Mg ⁇ 4.7 and Cu / Mg between 1.15 and 1.45.
- zirconium at 0.08 - 0.20% limits recrystallization. This role can also be fulfilled by other elements, such as chromium (0.05 - 0.40%), scandium (0.01 - 0.50%), hafhium (0.05 - 0, 60%) or vanadium (0.02 - 0.20%).
- a Zr content of not more than 0.15% is preferred to avoid the formation of primary phases.
- these anti-recrystallizing elements are added, their sum is limited by the appearance of the same phenomenon.
- only zirconium is added. Chromium is especially suitable for thin products. It is also possible to add up to 0.8% of manganese as an anti-recrystallizing element. In any event, it is preferable that the sum of the anti-recrystallizing elements does not exceed approximately 1%.
- This alloy is then cast according to one of the techniques known to a person skilled in the art to obtain a raw form, such as a spinning billet or a rolling plate.
- This raw form is then homogenized.
- the purpose of this heat treatment is threefold: (i) dissolve the coarse soluble phases formed on solidification (ii) reduce the concentration gradients in order to facilitate the dissolution step and (iii) precipitate the dispersoids in order to limit / eliminate the recrystallization phenomena during the dissolution step.
- the Applicant has found that the alloy according to the invention was characterized by a particularly low end-of-solidification temperature compared with alloys of the 7040, 7050 or 7475 type. The same is true of the temperature above which the partial melting of the alloy is observed.
- the homogenization is carried out in two stages, with a first stage between 452 and 473 ° C, typically for a period of between 4 and 30 hours (preferably between 4 and 15 hours), followed by a second stage between 465 and 484 ° C, and preferably between 467 and 481 ° C, typically for a period of between 4 and 30 hours (preferably between 4 and 16 hours).
- the first step is carried out between 457 and 463 ° C, and the second between 467 and 474 ° C.
- homogenization is carried out in a single step with a linear rise at 40 ° C per hour to a temperature between 467 and 481 ° C, preferably between 471 and 481 ° C, and typically during between 4 and 30 hours. It is also possible to make the homogenization in three stages. Homogenization can also be carried out in a single step, with a temperature rise of less than 200 ° C / h, and preferably between 20 and 50 ° C / h up to a plateau between 465 and 484 ° C, and preferably between 471 and 481 ° C.
- the raw form is then transformed hot to form extruded products (in particular bars, tubes or profiles), hot-rolled sheets or forgings.
- the spinning is preferably done at a die temperature between 380 and 430 ° C, and preferably between 390 and 420 ° C, by one of the methods known to those skilled in the art, such as direct spinning or reverse spinning. It is preferred that the hot transformation by spinning takes place with a block temperature of between 400 and 460 ° C., and preferably between 420 ° C. and 440 ° C. It is thus possible to obtain spun products which nowhere shows a coarse-grained cortical layer with a thickness greater than 3 mm, and preferably limited to 1 mm, in particular in the case of thinner spun products.
- the hot transformation can optionally be followed by a cold transformation.
- a cold transformation As an example, it is possible to manufacture spun and drawn tubes.
- the temperature is increased continuously for a period of between 2 and 6 hours, and preferably approximately 4 hours, up to a temperature between 470 and 500 ° C (preferably not exceeding 485 ° C), preferably between 474 and 484 ° C, and even more preferably between 477 and 483 ° C, and maintains the product at this temperature for a period of between 1 and 10 hours, and preferably approximately 2 to 4 hours.
- the products are soaked, preferably in a preferably liquid quenching medium such as water, said liquid preferably having a temperature not exceeding 40 ° C.
- the products can be subjected to a controlled traction with a permanent elongation of the order of 1 to 5%, and preferably 1.5 to 3%.
- a first step between 110 ° C and 130 ° C is suitable.
- the first level is between 115 ° C and 125 ° C.
- an equivalent TEQ treatment time (160 ° C.) of between 0J and 2 hours, and preferably between 0.1 and 0.5 hours, can be used.
- the second level is advantageously between 150 and 170 ° C.
- the equivalent TEQ treatment time (160 ° C) for this second stage is advantageously between 4 and 16 hours, and preferably between 6 and 12 hours. If we aim to optimize the compromise between Ro.
- a second longer bearing at a temperature between 150 ° C and 170 ° C is preferable, for example an equivalent TEQ treatment time (160 ° C) between 16 and 30 hours.
- the second stage was carried out at a temperature of 160 ° C. for 24 hours.
- the temperature of the second level is between 155 and 165 ° C.
- the control of the duration of this second stage is particularly important for the final properties of the product.
- the second level is between 157 and 163 ° C, and its duration is between 6 and 10 hours.
- the second level is carried out at a slightly lower temperature, between 150 and 160 ° C.
- a temperature of the order of 115 to 145 ° C. will advantageously be used for a duration of the order of 4 to 50 hours, for example 48 hours at 120 ° C.
- an equivalent TEQ treatment time (160 ° C.) of the order of 0.6 hours to 1.20 hours can be used.
- the static mechanical characteristics are typically measured in the longest leg of the profile.
- the samples for assessing tolerance to damage are taken from a flat area of sufficient width which includes, where possible, the longest branch, this area being commonly called the profile sole.
- samples were taken for the measurement of static mechanical characteristics at the depth recommended by standard EN 485-1: 1993 (clause 6.1.3.4.).
- the method according to the invention leads to new products which have particularly advantageous characteristics for aeronautical construction.
- These products can be in the form of sheets, in particular thick sheets, or sections, or forgings. More particularly, the present invention makes it possible to produce thick profiles which can be used as wing stiffeners.
- Those skilled in the art know that the choice of the width W of the test piece affects the value of K app obtained.
- K app ( L - ⁇ ) is substantially the same at around 20 ° C and at around -50 ° C, knowing that -50 ° C is a typical ambient temperature when flying a civilian jet aircraft. More precisely, this value of K app (L- ⁇ ) does not decrease by more than 3% when going from about 20 ° C to about -50 ° C. In a preferred embodiment of the present invention, it does not decrease at all. We know that in certain alloys of the 7xxx series, the toughness decreases with temperature.
- the product is an airfoil stiffener, which has the following set of properties (measured at mid-thickness and at a temperature of approximately 20 ° C.):
- the invention makes it possible to obtain a product which shows at least one set of properties (measured at around 20 ° C.) selected from the group formed by the five sets: (a) an elastic limit R p o. 2 ( L ) of at least 480 MPa (and preferably at least 500 MPa), a breaking strength R m (L) of at least 530 MPa (and preferably at least 555 MPa) and a K IC ( L - T ) of at least 36 MPa m (and preferably of at least 40 MPaVm and even more preferably of at least 44 MPaVm)
- a yield strength R p o.2 (L) of at least 550 MPa (and preferably at least 580 MPa, and even more preferably at least 600 MPa) and a Ka P p (- ⁇ ) measured with W 100 mm) of at least 80 MPaVm (and preferably of at least 83 MPa m, and even more preferably of at least 87 MPa m);
- an elastic limit R p o.2 ( L ) of at least 550 MPa (and preferably at least 580 MPa) and a crack propagation speed da / dn not exceeding 3 10 "3 mm / cycle (and preferably not exceeding 2.5 10 "3 mm / cycle) for ⁇ K 27 ;
- a breaking strength Rm (L) of at least 580 MPa (and preferably of at least 600 MPa and even more preferably of at least 620 MPa) and a K apP ( L - ⁇ ) measured with W 100 mm of at least 80 MPa m (and preferably at least 83 MPaVm, and even more preferably at least 87 MPaVm).
- such a product can additionally show at least one property selected from the group formed by: (a) an elongation at break A (> of at least 9%, and preferably at least 12% (b) an exfoliating corrosion resistance measured according to ASTM G34 of at least EB.
- the invention makes it possible above all to increase the tensile strength and the elastic limit, while maintaining the other properties of use at an at least comparable level.
- the reduction in elongation at break is not a drawback for these applications, which normally do not require a particularly high value; if there is in some cases a small drawback associated with this drop, it is very largely offset by the increase in mechanical strength.
- the product according to the invention is particularly suitable for the manufacture of structural elements whose effective width to be considered with regard to dimensioning in toughness or in cracking is limited by geometric factors of the structure in which these structural elements must be integrated, for example by a design which effectively limits the width of the panels excluding stiffeners.
- the optimal product according to the invention corresponds to that which offers the maximum static mechanical resistance while ensuring sufficient toughness to ensure that the residual resistance of the part in the presence of a crack is limited by the static resistance of the product, or even a combination of static mechanical strength and toughness, and not by its intrinsic toughness.
- a particularly preferred product according to the invention is a wing stiffener, obtained by spinning, for example a lower surface stiffener.
- Another advantageous product is a fuselage frame.
- spun products have been produced with a cortical layer (peripheral layer of recrystallized grains) at the center of the long branches which remains a) less than 3.0 mm whatever the section; or b) less than 1.5 mm for sections of width less than equal to 50mm, or c) less than e / 4 mm (where e is the thickness) for sections of width less than or equal to 10 mm.
- Another advantage of the product according to the invention is the possibility of income forming. We know that aeronautical structural elements must have precise shapes dictated by aerodynamics.
- These geometries can be obtained by cold forming.
- the alloy requires a tempering treatment, this can be carried out after shaping in order to benefit from a metal that is more ductile and easier to shape.
- These geometries can also be obtained by shaping during the heat treatment of tempering.
- the metal is delivered in an intermediate metallurgical state, typically after a first level of tempering. This advantageous process in terms of cost and reproducibility is only possible with products comprising an income treatment allowing effective shaping.
- the 2xxx T351x alloys used for the stiffeners and wing panels do not allow this process to be used since they do not undergo any income treatment.
- the product according to the invention is particularly suitable for the manufacture of structural elements which have to undergo an income forming during the second income level.
- the product according to the invention thanks to its compromise in properties, is very advantageous for applications which require both high mechanical strength and high tolerance with regard to occasional overloads without leading to sudden rupture of the part.
- the products according to the invention have been used for the manufacture of other parts or structural elements which meet high safety requirements.
- the applicant has manufactured by spinning, possibly followed by cold drawing, tubes for the production of frames, forks and handlebars for cycles (bicycles, tricyles, motorcycles, etc.), or baseball bats.
- it has been found to be advantageous to add to the alloy a low content of scandium and / or hafhium, for example between 0.15 and 0.60% of scandium and approximately 0.50% of hafhium.
- a manufacturing process is chosen which leads to a fiber structure of the tubes.
- Spinning billets of diameter 291 mm (alloy A) were cast by semi-continuous casting, the composition of which is indicated in Table 1. These billets were homogenized in two stages:
- the content of Cu, Mg and Zn was determined by chemical analysis after dissolution of part of the sample, while the other elements were determined by X-ray spectroscopy on solid.
- Profiles of section “I” were spun (see Figure 1: thickness of the order of 17 mm to 22 mm, width of the order of 160 mm and height of the order of 80 mm) from peeled billets with a diameter of 270 mm, at a plot temperature between 390 and 410 ° C and a container temperature between 400 and 420 ° C, with an exit speed of about 0.5 m / min.
- the profiles were dissolved by increasing the temperature continuously for 3 hours to 481 ⁇ 3 ° C and keeping them at this temperature for 6 hours, then soaked in water between 22 and 25 ° C and pulled with a permanent deformation of between 1.5 and 3%. An over-income treatment was then carried out to obtain products in the T76 state.
- the over-tempering was carried out in two stages: first at 120 ° C for 6 hours, then at 160 ° C for a variable duration.
- the thickness of the coarse-grained recrystallized layer measured at the center of the sole is less than 1 mm.
- their static mechanical characteristics R m , R p o, 2, A
- their resistance to stress corrosion according to ASTM G 47
- the latter was calculated using the maximum load measured during the test according to ASTM E561-98 on test pieces of width W equal to 100 mm, and the initial crack length (at the end of pre-cracking) in the formulas indicated
- Table 2 shows the influence of the duration of the second tempering stage on certain properties measured at the end of the profile; the mechanical characteristics having been measured at 20 ° C.
- the results of the tensile test were obtained on a test piece of circular section, diameter 10 mm, half-thickness and half-width in the long branch.
- the KIc toughness results were obtained on specimens taken at half-thickness and half-width in the long branch or the thickest branch.
- EXCO corrosion results were obtained on specimens taken at half thickness and half width in the branch.
- the Kapp results were obtained on mid-thickness test pieces and centered in the sole of the profile containing the long branch.
- the “Compact-tension panel” type samples were taken at mid-thickness and half-width of the sole at the end of the profile. Table 3:
- Corrosion test specimens under stress in a corrosive environment were taken at mid-thickness and half-width of the long branch at the end of the profile.
- the crack propagation in corrosive medium in the thickness direction was of the order of 5 10 "9 m / s for a second 8 hour tempering stage at 160 ° C.
- the products were dissolved with a rise in temperature in 35 min to 479 ⁇ 2 ° C, with a plateau of 4 hours at this temperature.
- the quenching was carried out in cold water.
- the flats were pulled with a permanent elongation of between 1.5 and 3%.
- the tempering was carried out in two stages: 6 hours at 120 ° C + 8 hours at 160 ° C.
- An ultrasonic check made it possible to verify the absence of internal faults (class AA MIL-STD-2154).
- the thickness of the coarse-grained recrystallized layer measured at the center of the sole is less than 1 mm.
- results of the tensile and compression test are collated in table 6.
- the results of the tensile test were obtained on a specimen of circular section, diameter 10 mm, at mid-thickness at the end of the flat and in two positions in the section: mid-width and edge.
- the results of the compression test were obtained on a test piece of circular section, diameter 10 mm, half-thick at the end of the flat and in two positions in the section: half-width and at the edge.
- Profiles of inverted 'T' section were spun (see Figure 3: thickness of the sole in the order of 25 mm, width of the reinforcement in the order of 40 mm, width of the sole in the order of 180 mm and height of the order of 70 mm) from billets of composition K (see example 2).
- the spinning conditions were similar to those of Example 2.
- Profiles X and Y underwent a solution similar to Example 2.
- Profile Z underwent a solution with a rise in temperature between 1 h and 2 h and a maintenance of 3 hours at 480 ⁇ 2 ° C.
- the three profiles were soaked in cold water and pulled between 1.5% and 3%.
- the profiles have been rectified to improve their straightness.
- the tempering was carried out in two stages with a first stage of 6 hours at 120 ° C.
- An ultrasonic test was carried out to verify the absence of internal faults (class A, MIL-STD-2154).
- the thickness of the coarse-grained recrystallized layer measured at the center of the sole is less than 1 mm.
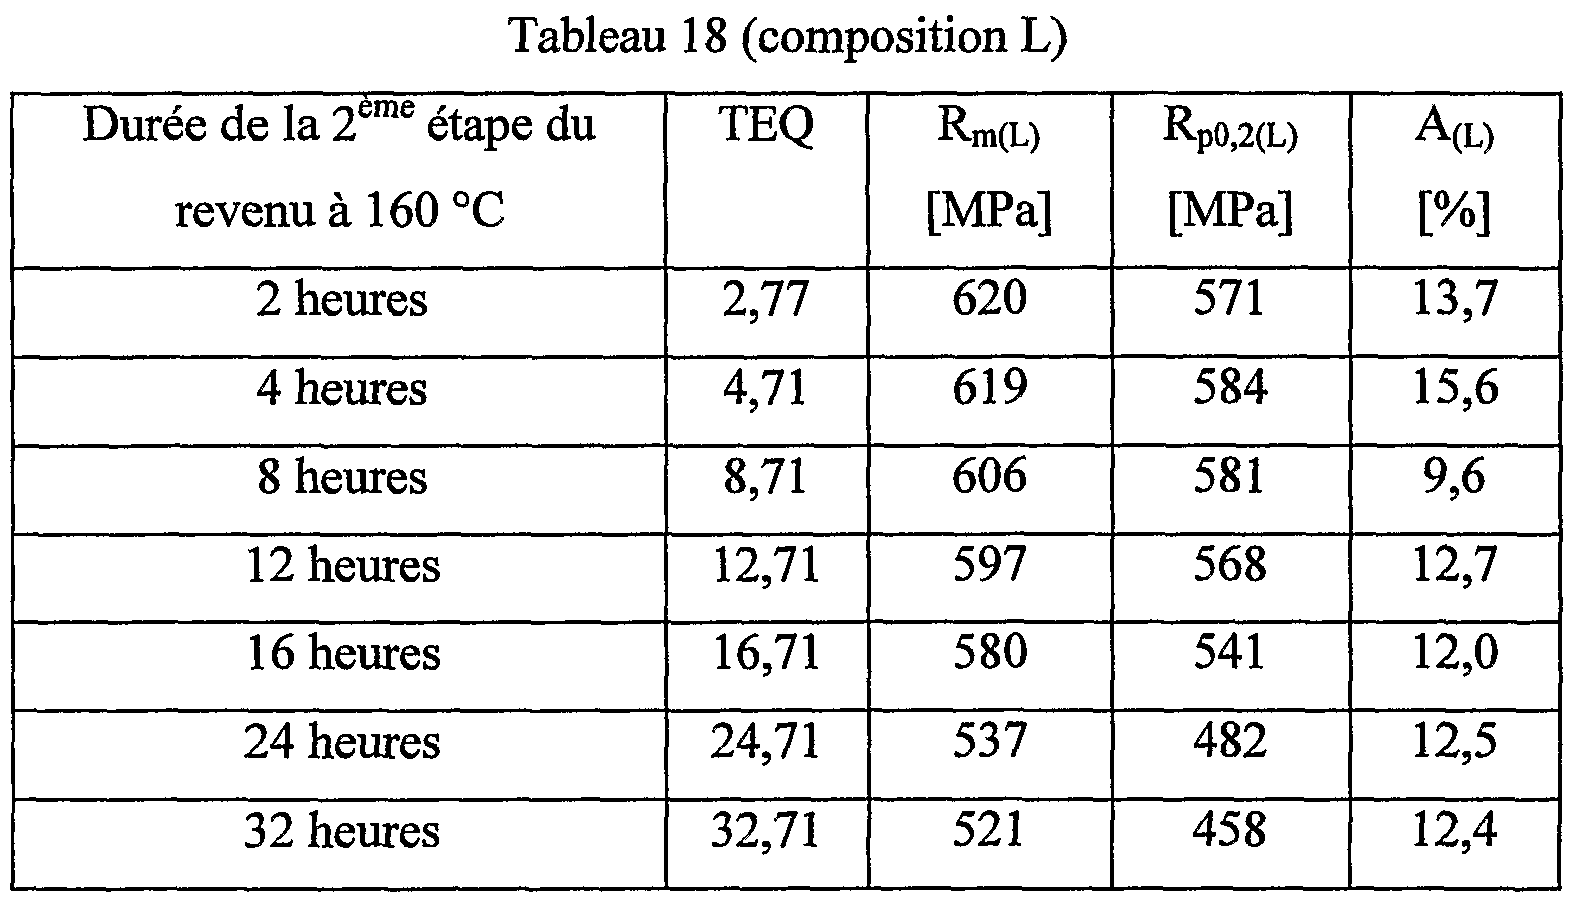
- Tables 11, 12 and 13 show the influence of the duration of the second tempering stage on certain product properties for the three profiles respectively X, Y and Z; the mechanical characteristics having been measured at 20 ° C.
- the test conditions are the same as those presented in Example 1.
- the results of the tensile test were obtained on a test piece of circular section, diameter 10 mm, at mid-thickness and half-width in the long branch .
- the KIc toughness and EXCO corrosion results were obtained on specimens taken at half-thickness and half-width in the long branch.
- the Kapp results were obtained on specimens centered in the sole of the profile containing the long branch.
- Corrosion corrosion test specimens were taken at the end of the profile at mid-thickness of the sole in two positions in the section: half-width of the long branch and half-width of the opposite branch in the sole.
- the products were dissolved with a temperature rise between 1 h and 2 h to 480 ⁇ 2 ° C, with a plateau of 3 hours at this temperature.
- the quenching was carried out in cold water between 21 and 22 ° C.
- the extradited and quenched sections were tensioned with a permanent elongation of between 1.5 and 3%.
- the profiles have been rectified to improve their straightness.
- a first income of 6 hours at 120 ° C was carried out.
- An ultrasonic test was carried out to verify the absence of internal faults (class A, MIL-STD-2154).
- a second tempering was carried out for 8 hours at 160 ° C.
- the thickness of the coarse-grained recrystallized layer measured at the center of the sole is less than 1 mm.
- Table 16 The results of the tensile test (on a test piece of circular section, diameter 10 mm, taken at the end of the profile, half-thickness and half-width in the long branch) are collated in Table 16. This table also contains the toughness and Kapp results both taken from the sole.
- the test conditions are the same as those presented in Example 1 except for the thickness B of the CCT specimen for the characterization of the Kapps which is 5 mm.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Heat Treatment Of Steel (AREA)
- Metal Extraction Processes (AREA)
- Extrusion Of Metal (AREA)
- Heat Treatment Of Articles (AREA)
- Conductive Materials (AREA)
- Forging (AREA)
Abstract
Description



Claims
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE04767427T DE04767427T1 (de) | 2003-06-24 | 2004-06-23 | Produkte aus al/zn/mg/cu-legierungen mit verbessertem kompromiss zwischen statischen mechanischen eigenschaften und schadenstoleranz |
| CA2528614A CA2528614C (fr) | 2003-06-24 | 2004-06-23 | Produits en alliages al-zn-mg-cu a compromis caracteristiques mecaniques statiques/tolerance aux dommages ameliore |
| EP04767427.0A EP1644546B1 (fr) | 2003-06-24 | 2004-06-23 | Utilisation de tubes en alliages al-zn-mg-cu ayant un compromis ameliore entre des caracteristiques mecaniques statiques et la tolerance aux dommages |
| BRPI0411873A BRPI0411873B1 (pt) | 2003-06-24 | 2004-06-23 | elementos de estrutura para construção aeronáutica, fabricado a partir de pelo menos um produto trefilado, laminado ou forjado em liga de alumínio e processo de fabricação |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US48074303P | 2003-06-24 | 2003-06-24 | |
| US60/480,743 | 2003-06-24 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| WO2005001149A2 true WO2005001149A2 (fr) | 2005-01-06 |
| WO2005001149A3 WO2005001149A3 (fr) | 2005-05-26 |
Family
ID=33551944
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/FR2004/001571 Ceased WO2005001149A2 (fr) | 2003-06-24 | 2004-06-23 | Produits en alliages al-zn-mg-cu a compromis caracteristiques mecaniques statiques/tolerance aux dommages ameliore |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US7452429B2 (fr) |
| EP (1) | EP1644546B1 (fr) |
| BR (1) | BRPI0411873B1 (fr) |
| CA (1) | CA2528614C (fr) |
| DE (1) | DE04767427T1 (fr) |
| WO (1) | WO2005001149A2 (fr) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR3071513A1 (fr) * | 2017-09-26 | 2019-03-29 | Constellium Issoire | Alliages al-zn-cu-mg a haute resistance et procede de fabrication |
| US10301710B2 (en) | 2005-01-19 | 2019-05-28 | Otto Fuchs Kg | Aluminum alloy that is not sensitive to quenching, as well as method for the production of a semi-finished product |
Families Citing this family (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| RU2345172C2 (ru) * | 2003-03-17 | 2009-01-27 | Корус Алюминиум Вальцпродукте Гмбх | Способ изготовления цельной монолитной алюминиевой конструкции и алюминиевое изделие, изготовленное путем механической обработки резанием из такой конструкции |
| EP1544315B1 (fr) * | 2003-12-16 | 2012-08-22 | Constellium France | Produit corroyé sous forme de tôle laminée et élément de structure pour aéronef en alliage Al-Zn-Cu-Mg |
| BRPI0606957B1 (pt) * | 2005-02-10 | 2016-09-13 | Alcan Rhenalu | produto trabalhado de liga à base de alumínio laminado ou forjado e processo para a sua produção |
| US8083871B2 (en) | 2005-10-28 | 2011-12-27 | Automotive Casting Technology, Inc. | High crashworthiness Al-Si-Mg alloy and methods for producing automotive casting |
| US8840737B2 (en) * | 2007-05-14 | 2014-09-23 | Alcoa Inc. | Aluminum alloy products having improved property combinations and method for artificially aging same |
| US8673209B2 (en) * | 2007-05-14 | 2014-03-18 | Alcoa Inc. | Aluminum alloy products having improved property combinations and method for artificially aging same |
| US8206517B1 (en) | 2009-01-20 | 2012-06-26 | Alcoa Inc. | Aluminum alloys having improved ballistics and armor protection performance |
| US8348785B2 (en) * | 2009-03-10 | 2013-01-08 | Fusheng Precision Co., Ltd. | Golf-club head having a striking plate made of high-strength aluminum alloy |
| US9163304B2 (en) | 2010-04-20 | 2015-10-20 | Alcoa Inc. | High strength forged aluminum alloy products |
| RU2569275C1 (ru) * | 2014-11-10 | 2015-11-20 | Федеральное государственное унитарное предприятие "Всероссийский научно-исследовательский институт авиационных материалов" (ФГУП "ВИАМ") | Плита из высокопрочного алюминиевого сплава и способ ее изготовления |
| DE102016001500A1 (de) * | 2016-02-11 | 2017-08-17 | Airbus Defence and Space GmbH | Al-Mg-Zn-Legierung für den integralen Aufbau von ALM-Strukturen |
| CA3032261A1 (fr) | 2016-08-26 | 2018-03-01 | Shape Corp. | Procede de formage a chaud et appareil de pliage transversal d'une poutre d'aluminium profilee pour former a chaud un composant structural de vehicule |
| CN110114498A (zh) | 2016-10-24 | 2019-08-09 | 形状集团 | 用于生产车辆零件的多阶段铝合金形成与热加工方法 |
| FR3068370B1 (fr) * | 2017-07-03 | 2019-08-02 | Constellium Issoire | Alliages al- zn-cu-mg et procede de fabrication |
| CN111876638B (zh) * | 2020-07-30 | 2022-01-11 | 中铝材料应用研究院有限公司 | 一种控制Al-Mg-Si-Mn合金中弥散粒子尺寸的热处理方法 |
| CN115821131B (zh) * | 2022-12-05 | 2024-05-14 | 山东南山铝业股份有限公司 | 一种低疲劳裂纹扩展速率2系铝合金型材及其制造方法 |
| CN115627396B (zh) * | 2022-12-08 | 2023-03-17 | 中国航发北京航空材料研究院 | 一种超高强韧、耐腐蚀的超长铝合金板材及其制备方法 |
Family Cites Families (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4305763A (en) * | 1978-09-29 | 1981-12-15 | The Boeing Company | Method of producing an aluminum alloy product |
| CA1173277A (fr) * | 1979-09-29 | 1984-08-28 | Yoshio Baba | Materiau pour lisses d'aeronef, et methode de production connexe |
| US4954188A (en) * | 1981-12-23 | 1990-09-04 | Aluminum Company Of America | High strength aluminum alloy resistant to exfoliation and method of making |
| FR2601967B1 (fr) | 1986-07-24 | 1992-04-03 | Cerzat Ste Metallurg | Alliage a base d'al pour corps creux sous pression. |
| US5312498A (en) * | 1992-08-13 | 1994-05-17 | Reynolds Metals Company | Method of producing an aluminum-zinc-magnesium-copper alloy having improved exfoliation resistance and fracture toughness |
| FR2695942B1 (fr) * | 1992-09-22 | 1994-11-18 | Gerzat Metallurg | Alliage d'aluminium pour corps creux sous pression. |
| US5865911A (en) * | 1995-05-26 | 1999-02-02 | Aluminum Company Of America | Aluminum alloy products suited for commercial jet aircraft wing members |
| FR2744136B1 (fr) | 1996-01-25 | 1998-03-06 | Pechiney Rhenalu | Produits epais en alliage alznmgcu a proprietes ameliorees |
| US6027582A (en) * | 1996-01-25 | 2000-02-22 | Pechiney Rhenalu | Thick alZnMgCu alloy products with improved properties |
| JPH11140610A (ja) * | 1997-11-13 | 1999-05-25 | Furukawa Electric Co Ltd:The | 靱性および溶接性に優れるアルミニウム合金構造材の製造方法 |
| FR2805282B1 (fr) * | 2000-02-23 | 2002-04-12 | Gerzat Metallurg | Procede de fabrication de corps creux sous pression en alliage a1znmgcu |
| IL156386A0 (en) * | 2000-12-21 | 2004-01-04 | Alcoa Inc | Aluminum alloy products and artificial aging method |
| US20050006010A1 (en) * | 2002-06-24 | 2005-01-13 | Rinze Benedictus | Method for producing a high strength Al-Zn-Mg-Cu alloy |
-
2004
- 2004-06-23 EP EP04767427.0A patent/EP1644546B1/fr not_active Expired - Lifetime
- 2004-06-23 US US10/873,635 patent/US7452429B2/en not_active Expired - Lifetime
- 2004-06-23 DE DE04767427T patent/DE04767427T1/de active Pending
- 2004-06-23 WO PCT/FR2004/001571 patent/WO2005001149A2/fr not_active Ceased
- 2004-06-23 CA CA2528614A patent/CA2528614C/fr not_active Expired - Lifetime
- 2004-06-23 BR BRPI0411873A patent/BRPI0411873B1/pt active IP Right Grant
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US10301710B2 (en) | 2005-01-19 | 2019-05-28 | Otto Fuchs Kg | Aluminum alloy that is not sensitive to quenching, as well as method for the production of a semi-finished product |
| FR3071513A1 (fr) * | 2017-09-26 | 2019-03-29 | Constellium Issoire | Alliages al-zn-cu-mg a haute resistance et procede de fabrication |
| WO2019063490A1 (fr) | 2017-09-26 | 2019-04-04 | Constellium Issoire | Alliages al-zn-cu-mg à haute résistance et procédé de fabrication |
| US12421578B2 (en) | 2017-09-26 | 2025-09-23 | Constellium Issoire | Al—Zn—Cu—Mg alloys with high strength and method of fabrication |
Also Published As
| Publication number | Publication date |
|---|---|
| EP1644546B1 (fr) | 2016-04-20 |
| CA2528614C (fr) | 2012-06-05 |
| WO2005001149A3 (fr) | 2005-05-26 |
| DE04767427T1 (de) | 2006-10-12 |
| BRPI0411873B1 (pt) | 2016-11-22 |
| US7452429B2 (en) | 2008-11-18 |
| CA2528614A1 (fr) | 2005-01-06 |
| EP1644546A2 (fr) | 2006-04-12 |
| BRPI0411873A (pt) | 2006-08-08 |
| US20050058568A1 (en) | 2005-03-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1644546B1 (fr) | Utilisation de tubes en alliages al-zn-mg-cu ayant un compromis ameliore entre des caracteristiques mecaniques statiques et la tolerance aux dommages | |
| EP2449142B1 (fr) | Alliage aluminium cuivre lithium a resistance mecanique et tenacite ameliorees | |
| EP1114877B1 (fr) | Element de structure d'avion en alliage Al-Cu-Mg | |
| CA2836531C (fr) | Alliage aluminium magnesium lithium a tenacite amelioree | |
| EP1492895B1 (fr) | Produits en alliages al-zn-mg-cu | |
| EP2655680B1 (fr) | Alliage aluminium cuivre lithium à résistance en compression et ténacité améliorées | |
| FR3068370B1 (fr) | Alliages al- zn-cu-mg et procede de fabrication | |
| CA3006871C (fr) | Alliage aluminium cuivre lithium a resistance mecanique et tenacite ameliorees | |
| FR2838135A1 (fr) | PRODUITS CORROYES EN ALLIAGES A1-Zn-Mg-Cu A TRES HAUTES CARACTERISTIQUES MECANIQUES, ET ELEMENTS DE STRUCTURE D'AERONEF | |
| EP2364378A1 (fr) | Produits en alliage aluminium-cuivre-lithium | |
| EP1544315B1 (fr) | Produit corroyé sous forme de tôle laminée et élément de structure pour aéronef en alliage Al-Zn-Cu-Mg | |
| FR2902442A1 (fr) | Alliage de la serie aa6xxx, a grande tolerance aux dommages pour l'industrie aerospatiale | |
| WO2009103899A1 (fr) | Produit lamine en alliage aluminium-lithium pour applications aeronautiques | |
| EP1891247B1 (fr) | Tole en aluminium-cuivre-lithium a haute tenacite pour fuselage d'avion | |
| EP3728667B1 (fr) | Procede de fabrication ameliore de tôles en alliage d'aluminium-cuivre-lithium pour la fabrication de fuselage d'avion et tôle correspondante | |
| CA2907807A1 (fr) | Toles en alliage d'aluminium-cuivre-lithium pour la fabrication de fuselages d'avion | |
| FR3057476A1 (fr) | Toles minces en alliage aluminium-magnesium-scandium pour applications aerospatiales | |
| FR2879217A1 (fr) | Toles fortes en alliage ai-zn-cu-mg a faibles contraintes internes | |
| CA2560672C (fr) | Element de structure pour construction aeronautique presentant une variation des proprietes d'emploi | |
| EP1544316A2 (fr) | Tôle épaisse en alliage Al-Zn-Cu-Mg recristallisée à faible teneur en Zr | |
| CA3058021A1 (fr) | Produits en alliage aluminium-cuivre-lithium | |
| FR3042508A1 (fr) | Toles minces en alliage aluminium-magnesium-zirconium pour applications aerospatiales |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| AK | Designated states |
Kind code of ref document: A2 Designated state(s): AE AG AL AM AT AU AZ BA BB BG BR BW BY BZ CA CH CN CO CR CU CZ DE DK DM DZ EC EE EG ES FI GB GD GE GH GM HR HU ID IL IN IS JP KE KG KP KR KZ LC LK LR LS LT LU LV MA MD MG MK MN MW MX MZ NA NI NO NZ OM PG PH PL PT RO RU SC SD SE SG SK SL SY TJ TM TN TR TT TZ UA UG US UZ VC VN YU ZA ZM ZW |
|
| AL | Designated countries for regional patents |
Kind code of ref document: A2 Designated state(s): GM KE LS MW MZ NA SD SL SZ TZ UG ZM ZW AM AZ BY KG KZ MD RU TJ TM AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LU MC NL PL PT RO SE SI SK TR BF BJ CF CG CI CM GA GN GQ GW ML MR NE SN TD TG |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application | ||
| WWE | Wipo information: entry into national phase |
Ref document number: 2528614 Country of ref document: CA |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2004767427 Country of ref document: EP |
|
| WWP | Wipo information: published in national office |
Ref document number: 2004767427 Country of ref document: EP |
|
| ENP | Entry into the national phase |
Ref document number: PI0411873 Country of ref document: BR |