WO2012164861A1 - 成形材料 - Google Patents
成形材料 Download PDFInfo
- Publication number
- WO2012164861A1 WO2012164861A1 PCT/JP2012/003299 JP2012003299W WO2012164861A1 WO 2012164861 A1 WO2012164861 A1 WO 2012164861A1 JP 2012003299 W JP2012003299 W JP 2012003299W WO 2012164861 A1 WO2012164861 A1 WO 2012164861A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- molding material
- weight
- phenol resin
- present
- resin
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L61/00—Compositions of condensation polymers of aldehydes or ketones; Compositions of derivatives of such polymers
- C08L61/04—Condensation polymers of aldehydes or ketones with phenols only
- C08L61/06—Condensation polymers of aldehydes or ketones with phenols only of aldehydes with phenols
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G73/00—Macromolecular compounds obtained by reactions forming a linkage containing nitrogen with or without oxygen or carbon in the main chain of the macromolecule, not provided for in groups C08G12/00 - C08G71/00
- C08G73/06—Polycondensates having nitrogen-containing heterocyclic rings in the main chain of the macromolecule
- C08G73/10—Polyimides; Polyester-imides; Polyamide-imides; Polyamide acids or similar polyimide precursors
- C08G73/1046—Polyimides containing oxygen in the form of ether bonds in the main chain
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G73/00—Macromolecular compounds obtained by reactions forming a linkage containing nitrogen with or without oxygen or carbon in the main chain of the macromolecule, not provided for in groups C08G12/00 - C08G71/00
- C08G73/06—Polycondensates having nitrogen-containing heterocyclic rings in the main chain of the macromolecule
- C08G73/10—Polyimides; Polyester-imides; Polyamide-imides; Polyamide acids or similar polyimide precursors
- C08G73/1046—Polyimides containing oxygen in the form of ether bonds in the main chain
- C08G73/1053—Polyimides containing oxygen in the form of ether bonds in the main chain with oxygen only in the tetracarboxylic moiety
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08G—MACROMOLECULAR COMPOUNDS OBTAINED OTHERWISE THAN BY REACTIONS ONLY INVOLVING UNSATURATED CARBON-TO-CARBON BONDS
- C08G73/00—Macromolecular compounds obtained by reactions forming a linkage containing nitrogen with or without oxygen or carbon in the main chain of the macromolecule, not provided for in groups C08G12/00 - C08G71/00
- C08G73/06—Polycondensates having nitrogen-containing heterocyclic rings in the main chain of the macromolecule
- C08G73/10—Polyimides; Polyester-imides; Polyamide-imides; Polyamide acids or similar polyimide precursors
- C08G73/1067—Wholly aromatic polyimides, i.e. having both tetracarboxylic and diamino moieties aromatically bound
- C08G73/1071—Wholly aromatic polyimides containing oxygen in the form of ether bonds in the main chain
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08K—Use of inorganic or non-macromolecular organic substances as compounding ingredients
- C08K7/00—Use of ingredients characterised by shape
- C08K7/02—Fibres or whiskers
- C08K7/04—Fibres or whiskers inorganic
- C08K7/06—Elements
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L79/00—Compositions of macromolecular compounds obtained by reactions forming in the main chain of the macromolecule a linkage containing nitrogen with or without oxygen or carbon only, not provided for in groups C08L61/00 - C08L77/00
- C08L79/04—Polycondensates having nitrogen-containing heterocyclic rings in the main chain; Polyhydrazides; Polyamide acids or similar polyimide precursors
- C08L79/08—Polyimides; Polyester-imides; Polyamide-imides; Polyamide acids or similar polyimide precursors
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L81/00—Compositions of macromolecular compounds obtained by reactions forming in the main chain of the macromolecule a linkage containing sulfur with or without nitrogen, oxygen or carbon only; Compositions of polysulfones; Compositions of derivatives of such polymers
- C08L81/06—Polysulfones; Polyethersulfones
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F04—POSITIVE - DISPLACEMENT MACHINES FOR LIQUIDS; PUMPS FOR LIQUIDS OR ELASTIC FLUIDS
- F04C—ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT MACHINES FOR LIQUIDS; ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT PUMPS
- F04C18/00—Rotary-piston pumps specially adapted for elastic fluids
- F04C18/02—Rotary-piston pumps specially adapted for elastic fluids of arcuate-engagement type, i.e. with circular translatory movement of co-operating members, each member having the same number of teeth or tooth-equivalents
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F04—POSITIVE - DISPLACEMENT MACHINES FOR LIQUIDS; PUMPS FOR LIQUIDS OR ELASTIC FLUIDS
- F04C—ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT MACHINES FOR LIQUIDS; ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT PUMPS
- F04C29/00—Component parts, details or accessories of pumps or pumping installations, not provided for in groups F04C18/00 - F04C28/00
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F04—POSITIVE - DISPLACEMENT MACHINES FOR LIQUIDS; PUMPS FOR LIQUIDS OR ELASTIC FLUIDS
- F04C—ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT MACHINES FOR LIQUIDS; ROTARY-PISTON, OR OSCILLATING-PISTON, POSITIVE-DISPLACEMENT PUMPS
- F04C2230/00—Manufacture
- F04C2230/20—Manufacture essentially without removing material
- F04C2230/21—Manufacture essentially without removing material by casting
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F05—INDEXING SCHEMES RELATING TO ENGINES OR PUMPS IN VARIOUS SUBCLASSES OF CLASSES F01-F04
- F05C—INDEXING SCHEME RELATING TO MATERIALS, MATERIAL PROPERTIES OR MATERIAL CHARACTERISTICS FOR MACHINES, ENGINES OR PUMPS OTHER THAN NON-POSITIVE-DISPLACEMENT MACHINES OR ENGINES
- F05C2225/00—Synthetic polymers, e.g. plastics; Rubber
- F05C2225/12—Polyetheretherketones, e.g. PEEK
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F05—INDEXING SCHEMES RELATING TO ENGINES OR PUMPS IN VARIOUS SUBCLASSES OF CLASSES F01-F04
- F05C—INDEXING SCHEME RELATING TO MATERIALS, MATERIAL PROPERTIES OR MATERIAL CHARACTERISTICS FOR MACHINES, ENGINES OR PUMPS OTHER THAN NON-POSITIVE-DISPLACEMENT MACHINES OR ENGINES
- F05C2231/00—Organic materials not otherwise provided for
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F05—INDEXING SCHEMES RELATING TO ENGINES OR PUMPS IN VARIOUS SUBCLASSES OF CLASSES F01-F04
- F05C—INDEXING SCHEME RELATING TO MATERIALS, MATERIAL PROPERTIES OR MATERIAL CHARACTERISTICS FOR MACHINES, ENGINES OR PUMPS OTHER THAN NON-POSITIVE-DISPLACEMENT MACHINES OR ENGINES
- F05C2253/00—Other material characteristics; Treatment of material
- F05C2253/04—Composite, e.g. fibre-reinforced
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F05—INDEXING SCHEMES RELATING TO ENGINES OR PUMPS IN VARIOUS SUBCLASSES OF CLASSES F01-F04
- F05C—INDEXING SCHEME RELATING TO MATERIALS, MATERIAL PROPERTIES OR MATERIAL CHARACTERISTICS FOR MACHINES, ENGINES OR PUMPS OTHER THAN NON-POSITIVE-DISPLACEMENT MACHINES OR ENGINES
- F05C2253/00—Other material characteristics; Treatment of material
- F05C2253/20—Resin
Definitions
- the present invention relates to a molding material.
- phenol resin molding materials excellent in heat resistance, dimensional stability, moldability and the like are used in key industries such as the automobile field, the electric field, and the electronic field.
- glass fiber reinforced phenolic resin is used as an alternative to metal part materials, and thus can be significantly reduced in cost, and therefore, active alternative studies have been conducted (for example, Patent Document 2).
- the current glass fiber reinforced phenolic resin molding material may be insufficient as a molding material for a scroll compressor because it may lack strength and elastic modulus to be used as a scroll compressor material for automobiles.
- a phenolic resin molding material having properties such as bending strength, flexural modulus, and toughness.
- the present invention has been made in view of such circumstances, and provides a molding material having improved specific strength and specific elastic modulus and excellent molding characteristics.
- the present invention also provides, for example, a molding material having a specific strength and a specific elastic modulus sufficient to be used as a material for a scroll compressor for automobiles and having excellent molding characteristics.
- a molding material containing a phenol resin, carbon fiber, polyethersulfone and / or polyetherimide is provided.
- the phenol resin is at least one selected from the group consisting of a novolac type phenol resin, a resol type phenol resin, and an aryl alkylene type phenol resin.
- the carbon fiber is a pitch-based or PAN-based carbon fiber.
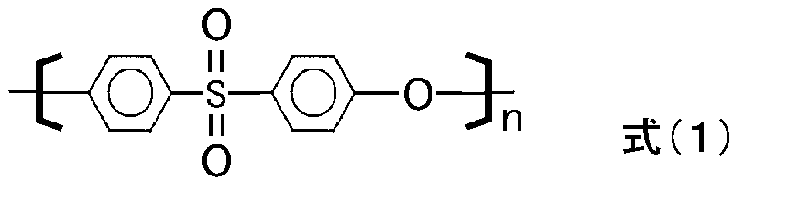
- the polyethersulfone resin in the molding material, has a structure represented by the formula (1).
- n is an integer of 1 or more
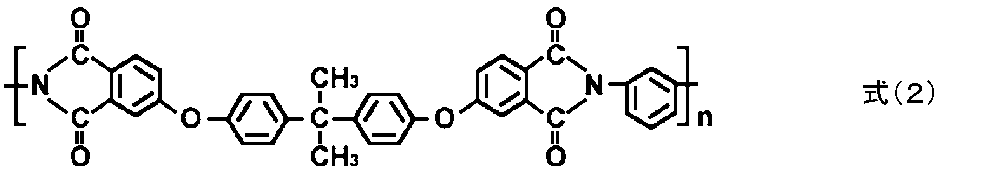
- the polyetherimide resin in the molding material, has a structure represented by the formula (2).
- n is an integer of 1 or more
- the phenol resin is in an amount of 25% by weight to 64% by weight with respect to the total weight of the molding material.
- the carbon fiber in the molding material, is in an amount of 20% by weight to 60% by weight with respect to the total weight of the molding material.
- the polyethersulfone in the molding material, is in an amount of 0.1 wt% or more and 20 wt% or less with respect to the total weight of the molding material.
- a molding material having improved specific strength and specific elastic modulus and excellent molding characteristics is provided.
- the molding material according to the present invention contains phenol resin, carbon fiber, and polyethersulfone or polyetherimide.
- phenolic resin used in the present invention examples include novolac type phenolic resin, resol type phenolic resin, arylalkylene type phenolic resin and the like.
- the novolak-type phenol resin used in the present invention can be obtained, for example, by reacting phenols and aldehydes under an acidic catalyst.
- phenols used for the production of novolak type phenol resins include phenol, cresol, xylenol, ethylphenol, p-phenylphenol, p-tert-butylphenol, p-tert-amylphenol, p-octylphenol, and p-nonylphenol. , P-cumylphenol, bisphenol A, bisphenol F, resorcinol and the like. These can be used alone or in combination of two or more.
- aldehydes used in the production of novolak type phenol resins include alkyl aldehydes such as formaldehyde, acetaldehyde, propyl aldehyde, and butyraldehyde, and aromatic aldehydes such as benzaldehyde and salicyl aldehyde.
- alkyl aldehydes such as formaldehyde, acetaldehyde, propyl aldehyde, and butyraldehyde
- aromatic aldehydes such as benzaldehyde and salicyl aldehyde.
- formaldehyde source include formalin (aqueous solution), paraformaldehyde, hemi-formal with alcohols, and trioxane. These can be used alone or in combination of two or more.
- the reaction molar ratio of phenols to aldehydes is usually 0.3 to 1.0 mol, particularly 0.6 to 0, per mol of phenol. .9 mol is preferable.
- the acidic catalyst examples include organic carboxylic acids such as oxalic acid and acetic acid, organic sulfonic acids such as benzenesulfonic acid, paratoluenesulfonic acid and methanesulfonic acid, 1-hydroxyethylidene-1,1′-diphosphonic acid, 2- Examples thereof include organic phosphonic acids such as phosphonobutane-1,2,4-tricarboxylic acid, inorganic acids such as hydrochloric acid, sulfuric acid and phosphoric acid. In addition, these acidic catalysts can also be used individually or in combination of 2 or more types.
- the resol type phenol resin used in the present invention is obtained by reacting phenols with aldehydes.
- phenols used in the production of the resol type phenolic resin of the present invention include cresols such as phenol, o-cresol, m-cresol, p-cresol, 2,3-xylenol, 2,4-xylenol, 2, Xylenols such as 5-xylenol, 2,6-xylenol, 3,4-xylenol, 3,5-xylenol, ethylphenols such as o-ethylphenol, m-ethylphenol, p-ethylphenol, isopropylphenol, butylphenol , Butylphenols such as p-tert-butylphenol, p-tert-amylphenol, p-octylphenol, p-nonylphenol, alkylphenols such as p-cumylphenol, fluorophenol, chlorophenol, bromophenol Halogenated phenols such as iod
- aldehydes used in the production of the resol type phenolic resin of the present invention include formaldehyde, paraformaldehyde, trioxane, acetaldehyde, propionaldehyde, polyoxymethylene, chloral, hexamethylenetetramine, furfural, glyoxal, n-butyraldehyde, Examples include proaldehyde, allyl aldehyde, benzaldehyde, crotonaldehyde, acrolein, tetraoxymethylene, phenylacetaldehyde, o-tolualdehyde, and salicylaldehyde. These can be used alone or in combination of two or more. Among these aldehydes, preferred are those selected from formaldehyde and paraformaldehyde, which are excellent in reactivity and inexpensive.
- a method for synthesizing the resol type phenol resin used in the present invention there may be mentioned a method in which the above-described phenols and aldehydes are reacted in the presence of a catalyst such as an alkali metal, an amine or a divalent metal salt.
- a catalyst such as an alkali metal, an amine or a divalent metal salt.
- Examples of the catalyst used when synthesizing the resol type phenol resin used in the present invention include alkali metal hydroxides such as sodium hydroxide, lithium hydroxide and potassium hydroxide, and alkaline earth metals such as calcium, magnesium and barium. And amines such as sodium carbonate, aqueous ammonia, triethylamine and hexamethylenetetramine, and divalent metal salts such as magnesium acetate and zinc acetate. These can be used alone or in combination of two or more.
- the reaction molar ratio of phenols to aldehydes is preferably 0.80 to 2.50 moles of aldehydes per mole of phenols. More preferably, the amount is 1.00 to 2.30 mol of aldehydes. If the molar ratio is less than the lower limit, a resol-type resin may not be obtained, and if the molar ratio exceeds the upper limit, reaction control may be difficult.
- the arylalkylene type phenol resin used in the present invention refers to an epoxy resin having one or more arylalkylene groups in a repeating unit.
- aryl alkylene type phenol resins include xylylene type epoxy resins and biphenyl dimethylene type epoxy resins. Among these, a biphenyl dimethylene type epoxy resin is preferable.
- the carbon fiber used in the present invention is pitch-based carbon fiber or PAN-based carbon fiber. These carbon fibers may be used alone or in combination of two or more.
- the shape of the carbon fiber used is not particularly limited, but a circular shape is preferable from the viewpoint of strength.
- the fiber diameter of the carbon fiber to be used is preferably 5 ⁇ m or more and 13 ⁇ m or less, more preferably 6 ⁇ m or more and 10 ⁇ m or less.
- the polyether sulfone used in the present invention commercially available products can be used.
- the polyethersulfone preferably contains a repeating unit represented by the following formula (1).
- n is an integer of 1 or more.
- n is 1 or more and 500 or less, more preferably 100 or more and 300 or less.
- polyetherimide used in the present invention those generally used in the field having a structure represented by the following formula (2) can be used.
- n is an integer of 1 or more.
- Either polyethersulfone or polyetherimide may be used alone or in combination.
- the weight of the phenol resin with respect to the total weight of the molding material is preferably 25% by weight to 64% by weight, more preferably 30% by weight to 60% by weight, and further preferably 35% by weight to 50% by weight. . If the upper limit is exceeded, blistering may occur in the resulting molded product, and if it is less than the lower limit, it may take time to cure and curing may be insufficient. Further, by setting the weight of the phenol resin to 30.5 wt% or more and 55 wt% or less with respect to the total weight of the molding material, it is possible to obtain a specific strength and a specific elastic modulus sufficient for use as a scroll.
- the weight of the carbon fiber with respect to the total weight of the molding material is preferably 20% by weight to 60% by weight, and more preferably 40% by weight to 55% by weight.
- the weight of the carbon fiber with respect to the total weight of a molding material is 35 to 55 weight%.
- the weight of polyethersulfone with respect to the total weight of the molding material is preferably 0.1% by weight to 20% by weight, more preferably 2% by weight to 8% by weight.
- the obtained molded article can have excellent specific strength and specific elastic modulus.
- the weight of polyethersulfone with respect to the total weight of a molding material is 0.5 to 15 weight%. Within the above range, it is possible to obtain a specific strength and a specific elastic modulus sufficient for use as a scroll.
- the molding material of the present invention may further contain components such as a mold release agent, a lubricant, a curing aid, a pigment, an inorganic filler, an elastomer, and glass fiber as necessary.
- inorganic fillers include silicates such as talc, fired clay, unfired clay, mica, oxides such as titanium oxide, alumina, silica, and fused silica, and carbonates such as calcium carbonate, magnesium carbonate, and hydrotalcite.
- Salts hydroxides such as aluminum hydroxide, magnesium hydroxide, calcium hydroxide, sulfates or sulfites such as barium sulfate, calcium sulfate, calcium sulfite, zinc borate, barium metaborate, aluminum borate, calcium borate And borate salts such as sodium borate, nitrides such as aluminum nitride, boron nitride, and silicon nitride, and glass fibers.
- glass fiber is preferable. When glass fiber is used, the mechanical strength of the obtained molded product can be maintained.
- the glass constituting the glass fiber is not particularly limited, and examples thereof include E glass, C glass, A glass, S glass, D glass, NE glass, T glass, and H glass. Among these, E glass, T glass, or S glass is preferable. Thereby, the high elasticity of glass fiber can be achieved and a thermal expansion coefficient can also be made small.
- the elastomer examples include acrylic acid-alkylstyrene copolymer, polyvinyl acetate, styrene-isoprene copolymer, acrylonitrile-budadiene copolymer, isoprene rubber, styrene-butadiene copolymer, ether-urethane copolymer, Examples thereof include a methyl-urethane copolymer, an ester-urethane copolymer, a vinyl-silicone copolymer, a phenyl-silicone copolymer, and a chloroprene copolymer.
- acrylic acid-alkylstyrene copolymers and acrylonitrile-budadiene copolymers are preferable because they have a wide application range and are easy to handle.
- the method for producing the molding material of the present invention is not particularly limited, but it is produced by mixing the above components and crushing the kneaded material heated and kneaded with a pressure kneader, a twin screw extruder, a heating roll, etc., with a power mill or the like. .
- the molding material thus obtained can be applied to injection molding, transfer molding, compression molding and the like to obtain a molded product having a desired shape.
- a raw material mixture containing 1% by weight of magnesium oxide, 1% by weight of a release agent and 1% by weight of a colorant is melt-kneaded for 3 minutes with a heating roll at 90 ° C., taken out, pulverized, and pulverized into granules. Obtained material.
- Test pieces were prepared by injection molding using the molding materials obtained in the examples and comparative examples.
- the molding conditions were a mold temperature of 175 ° C. and a curing time of 1 minute.
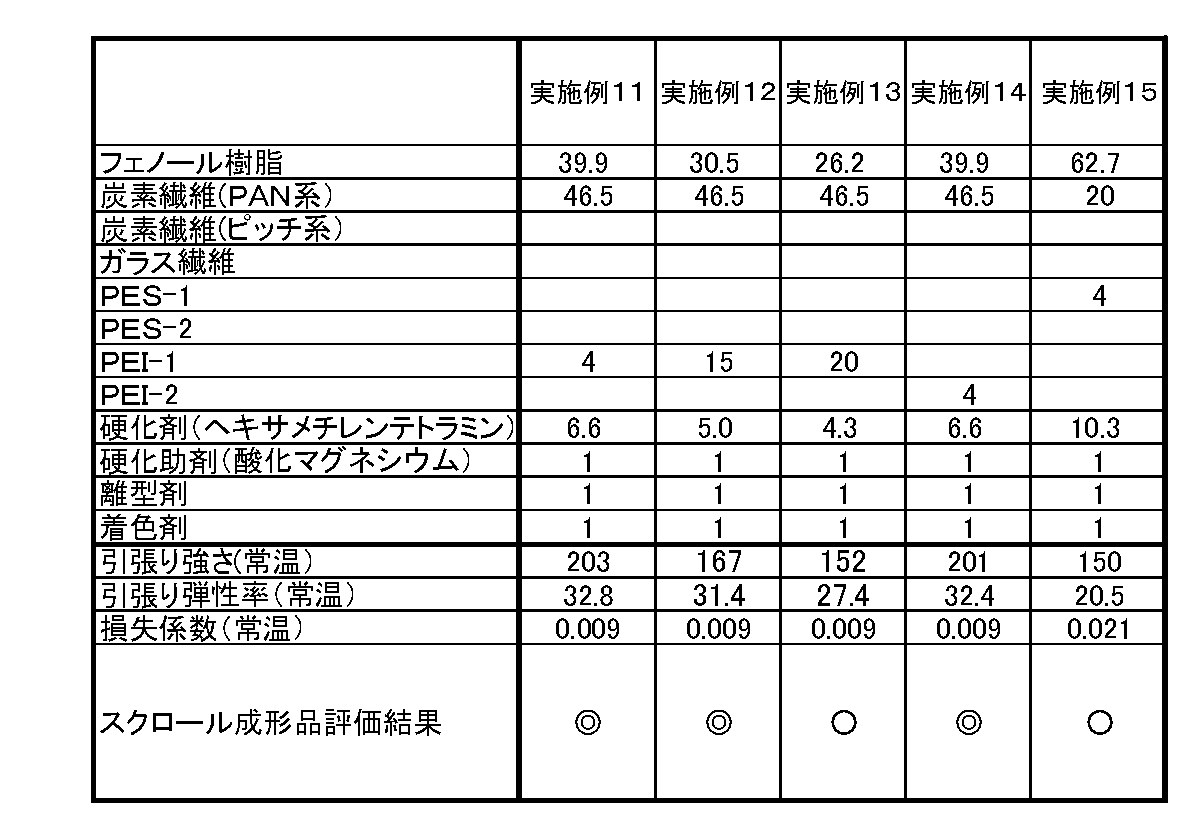
- test piece was treated in a 180 ° C. atmosphere for 6 hours, and the tensile strength (room temperature), tensile modulus (room temperature), and loss factor (room temperature) were set in JIS K 6911 “General Thermosetting Plastic Testing Method”. Measured in conformity.
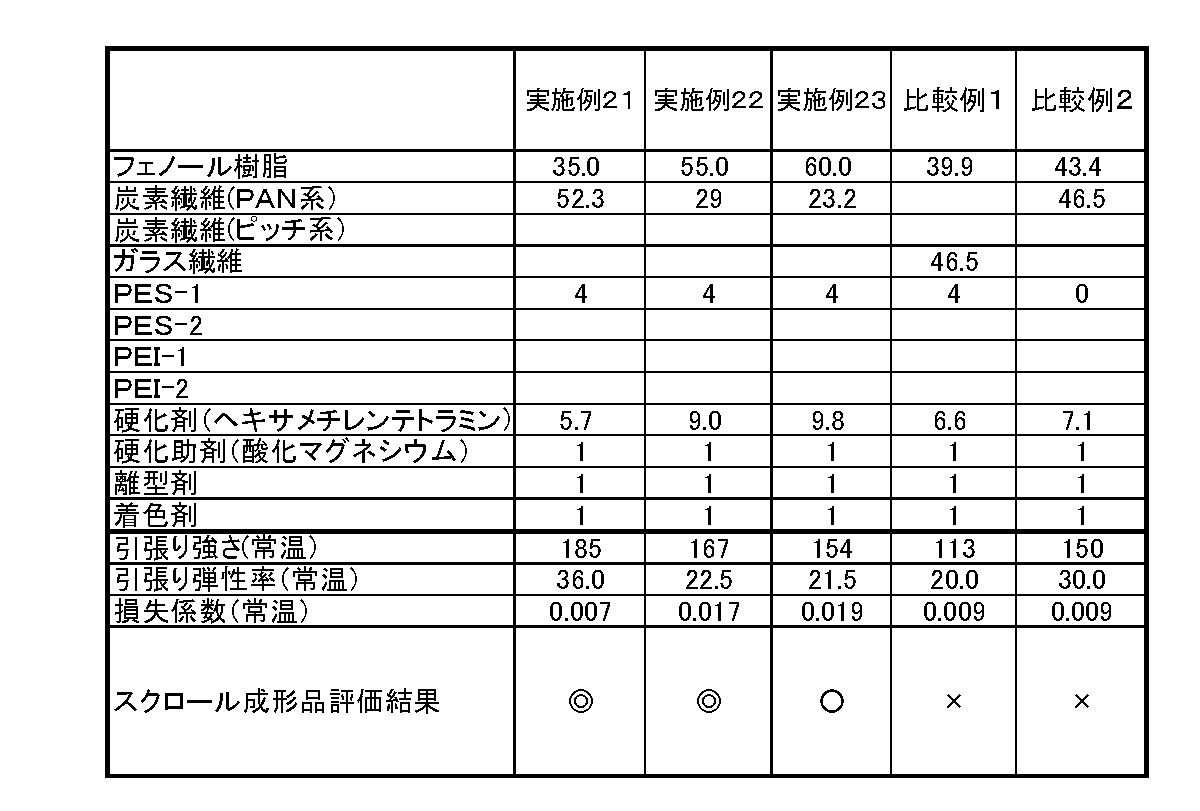
- Example 1 Using the components shown in Table 1, a molding material was obtained by using the same method as in Example 1. The amounts of the components shown in Table 1 are all weight percent. In addition, the component of Table 1 used the following.
- Phenolic resin novolac type phenolic resin
- PR-HF-3 Synitomo Bakelite
- Glass fiber E glass fiber manufactured by Nittobo Co., Ltd.
- PES-1 polyethersulfone
- PES-2 polyethersulfone
- PEI-1 polyetherimide
- PEI-2 polyetherimide
- ULTEM 1040A manufactured by SABIC Innovative Plastics
- Curing agent hexamethylenetetramine
- Curing aid Magnesium oxide
- Release agent Calcium stearate
- Colorant Carbon black
Landscapes
- Chemical & Material Sciences (AREA)
- Health & Medical Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Organic Chemistry (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Compositions Of Macromolecular Compounds (AREA)
- Rotary Pumps (AREA)
Abstract
Description
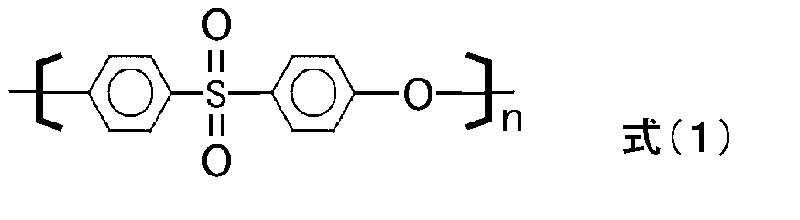
(式(1)中、nは1以上の整数である)
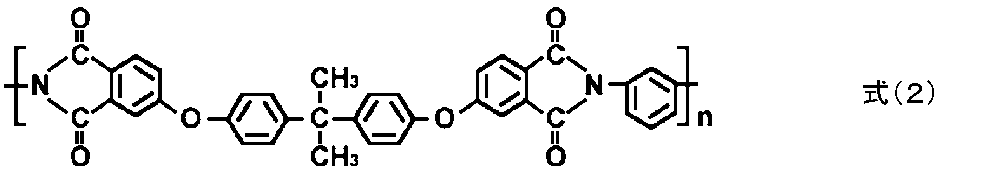
(式(2)中、nは1以上の整数である)
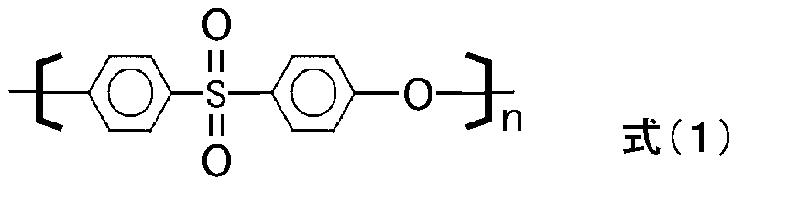
式(1)中、nは1以上の整数である。好ましくは、nは、1以上500以下であり、より好ましくは100以上300以下である。

(式(2)中、nは1以上の整数である)。
実施例及び比較例で得られた成形材料を用いて、インジェクション成形により試験片を作製した。成形条件は、金型温度175℃、硬化時間1分間とした。
(2)炭素繊維(PAN系):東邦テナックス社製 HT C261 6mm
(3)炭素繊維(ピッチ系):三菱樹脂社製 DIALEAD K223SE
(4)ガラス繊維: 日東紡績社製 Eガラス繊維
(5)PES-1(ポリエーテルスルホン):住友化学社製 5003PS
(6)PES-2(ポリエーテルスルホン):住友化学社製 4800P
(7)PEI-1(ポリエーテルイミド):SABICイノベーティブプラスチック社製 Ultem1000
(8)PEI-2(ポリエーテルイミド):SABICイノベーティブプラスチック社製 Ultem1040A
(9)硬化剤(ヘキサメチレンテトラミン): 住友精化社製 ウロトロピン
(10)硬化助剤: 酸化マグネシウム
(11)離型剤 : ステアリン酸カルシウム
(12)着色剤 : カーボンブラック
結果を以下の表にまとめて示す。



Claims (8)
- フェノール樹脂と、
炭素繊維と、
ポリエーテルスルホンおよび/またはポリエーテルイミドと、
を含む、成形材料。 - 前記フェノール樹脂が、ノボラック型フェノール樹脂、レゾール型フェノール樹脂、およびアリールアルキレン型フェノール樹脂からなる群から選択される少なくとも1つである、請求項1に記載の成形材料。
- 前記炭素繊維が、ピッチ系またはPAN系の炭素繊維である、請求項1に記載の成形材料。
- 前記ポリエーテルスルホンが、式(1)で示される構造を有する、請求項1に記載の成形材料。
(式(1)中、nは1以上の整数である) - 前記ポリエーテルイミドが、式(2)で示される構造を有する、請求項1に記載の成形材料。
(式(2)中、nは1以上の整数である) - 前記フェノール樹脂が、前記成形材料の全重量に対して、25重量%以上64重量%以下の量である、請求項1に記載の成形材料。
- 前記炭素繊維が、前記成形材料の全重量に対して、20重量%以上60重量%以下の量である、請求項1に記載の成形材料。
- 前記ポリエーテルスルホンが、前記成形材料の全重量に対して、0.1重量%以上20重量%以下の量である、請求項1に記載の成形材料。
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US14/123,364 US20140107281A1 (en) | 2011-05-31 | 2012-05-21 | Molding material |
| EP12792347.2A EP2716708A4 (en) | 2011-05-31 | 2012-05-21 | FABRIC |
| KR1020137033759A KR20140034840A (ko) | 2011-05-31 | 2012-05-21 | 성형 재료 |
| CA2837681A CA2837681A1 (en) | 2011-05-31 | 2012-05-21 | Molding material |
| CN201280026145.8A CN103562307A (zh) | 2011-05-31 | 2012-05-21 | 成型材料 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2011-121343 | 2011-05-31 | ||
| JP2011121343A JP5715884B2 (ja) | 2011-05-31 | 2011-05-31 | スクロール成形品 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2012164861A1 true WO2012164861A1 (ja) | 2012-12-06 |
Family
ID=47258738
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2012/003299 Ceased WO2012164861A1 (ja) | 2011-05-31 | 2012-05-21 | 成形材料 |
Country Status (8)
| Country | Link |
|---|---|
| US (1) | US20140107281A1 (ja) |
| EP (1) | EP2716708A4 (ja) |
| JP (1) | JP5715884B2 (ja) |
| KR (1) | KR20140034840A (ja) |
| CN (1) | CN103562307A (ja) |
| CA (1) | CA2837681A1 (ja) |
| TW (1) | TW201311795A (ja) |
| WO (1) | WO2012164861A1 (ja) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2014237300A (ja) * | 2013-06-10 | 2014-12-18 | 三菱重工業株式会社 | 樹脂構造体並びに該樹脂構造体を含む樹脂製スクロール流体機械 |
| US11285221B2 (en) | 2014-06-16 | 2022-03-29 | Mayo Foundation For Medical Education And Research | Treating myelomas |
Families Citing this family (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP5876007B2 (ja) | 2013-05-31 | 2016-03-02 | 三菱電線工業株式会社 | 樹脂組成物およびそれを用いたシール部材 |
| CN103580310B (zh) * | 2013-10-10 | 2017-09-22 | 张宏峰 | 盘式发电机 |
| JP6170426B2 (ja) * | 2013-12-24 | 2017-07-26 | 株式会社デンソー | スクロール型圧縮機構 |
| JP6831175B2 (ja) * | 2015-10-29 | 2021-02-17 | 住友ベークライト株式会社 | フェノール樹脂成形材料 |
| JP6203873B2 (ja) * | 2016-01-20 | 2017-09-27 | 三菱電線工業株式会社 | 樹脂組成物およびそれを用いたシール部材 |
| CN110249133B (zh) * | 2017-02-09 | 2021-03-26 | 三菱电机株式会社 | 旋转型压缩机 |
| US10677759B2 (en) * | 2017-10-26 | 2020-06-09 | The Boeing Company | Adhesive additive with enhanced stiffness change and non-destructive inspection method |
| US20190127615A1 (en) * | 2017-10-26 | 2019-05-02 | The Boeing Company | Adhesive with Enhanced Stiffness Change and Methods of Joining Composite Parts |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01500274A (ja) * | 1987-02-12 | 1989-02-02 | ゼネラル・エレクトリック・カンパニイ | ポリエーテルイミド―ポリアミド組成物 |
| JPH04283256A (ja) * | 1991-03-12 | 1992-10-08 | Sumitomo Chem Co Ltd | 熱可塑性樹脂変性ノボラック樹脂組成物及びその製造方法 |
| JP2000169669A (ja) | 1998-12-07 | 2000-06-20 | Zexel Corp | コンプレッサ―用部材及びその製造方法並びにスクロ―ルコンプレッサ― |
| JP2002129005A (ja) * | 2000-10-30 | 2002-05-09 | Sumitomo Bakelite Co Ltd | ポリエーテル芳香族ケトン系樹脂組成物並びにフィルム及びシート |
| JP2005281364A (ja) | 2004-03-29 | 2005-10-13 | Sumitomo Bakelite Co Ltd | フェノール樹脂成形材料 |
| JP3915045B2 (ja) | 1997-03-31 | 2007-05-16 | フドー株式会社 | マシニングセンタにおける構造部品成形材料、及びマシニングセンタにおける構造部品成形体 |
| WO2009031243A1 (ja) * | 2007-09-08 | 2009-03-12 | Toho Tenax Co., Ltd. | 繊維強化プリプレグ及びそれから得られる複合材料 |
| JP2011068778A (ja) * | 2009-09-25 | 2011-04-07 | Yokohama Rubber Co Ltd:The | 熱硬化性樹脂組成物 |
| JP2011099094A (ja) * | 2009-10-05 | 2011-05-19 | Yokohama Rubber Co Ltd:The | 繊維強化複合材料用エポキシ樹脂組成物、これを用いるプリプレグおよびハニカムサンドイッチパネル |
| JP2011213991A (ja) * | 2010-03-16 | 2011-10-27 | Toray Ind Inc | 炭素繊維強化複合材料 |
Family Cites Families (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2970121A (en) * | 1957-07-03 | 1961-01-31 | Union Carbide Corp | Molding composition comprising a novolac resin, a furan derivative, and a filler, and process for making same |
| JPH03275764A (ja) * | 1990-03-26 | 1991-12-06 | Asahi Chem Ind Co Ltd | 潤滑性樹脂組成物 |
| JP3182967B2 (ja) * | 1992-03-02 | 2001-07-03 | 東レ株式会社 | クロスプリプレグ |
| EP0957129B1 (en) * | 1997-12-03 | 2004-03-10 | Toray Industries, Inc. | Phenolic resin composition for fiber-reinforced composite material, prepreg for fiber-reinforced composite material, and process for producing prepreg for fiber-reinforced composite material |
| CN100483812C (zh) * | 2006-01-25 | 2009-04-29 | 中国科学院大连化学物理研究所 | 氧化还原液流储能电池用一体化电极双极板及其制备 |
| JP4141481B2 (ja) * | 2006-04-25 | 2008-08-27 | 横浜ゴム株式会社 | 繊維強化複合材料用エポキシ樹脂組成物 |
| US9416465B2 (en) * | 2006-07-14 | 2016-08-16 | Sabic Global Technologies B.V. | Process for making a high heat polymer fiber |
| JP4969363B2 (ja) * | 2006-08-07 | 2012-07-04 | 東レ株式会社 | プリプレグおよび炭素繊維強化複合材料 |
| CN101007443B (zh) * | 2007-01-26 | 2010-09-01 | 北京化工大学 | 纳米纤维增韧碳纤维树脂基复合材料的制备方法 |
| JP2008248462A (ja) * | 2007-03-06 | 2008-10-16 | Teijin Ltd | ピッチ系炭素繊維フィラー及びそれを用いた成形体 |
| EP2481777B1 (en) * | 2009-09-25 | 2017-10-25 | The Yokohama Rubber Co., Ltd. | Thermosetting resin composition, thermosetting resin composition for fiber-reinforced composite material, prepreg using the same, and honeycomb sandwich panel |
-
2011
- 2011-05-31 JP JP2011121343A patent/JP5715884B2/ja not_active Expired - Fee Related
-
2012
- 2012-05-21 EP EP12792347.2A patent/EP2716708A4/en not_active Withdrawn
- 2012-05-21 KR KR1020137033759A patent/KR20140034840A/ko not_active Withdrawn
- 2012-05-21 WO PCT/JP2012/003299 patent/WO2012164861A1/ja not_active Ceased
- 2012-05-21 CA CA2837681A patent/CA2837681A1/en not_active Abandoned
- 2012-05-21 CN CN201280026145.8A patent/CN103562307A/zh active Pending
- 2012-05-21 US US14/123,364 patent/US20140107281A1/en not_active Abandoned
- 2012-05-28 TW TW101118934A patent/TW201311795A/zh unknown
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01500274A (ja) * | 1987-02-12 | 1989-02-02 | ゼネラル・エレクトリック・カンパニイ | ポリエーテルイミド―ポリアミド組成物 |
| JPH04283256A (ja) * | 1991-03-12 | 1992-10-08 | Sumitomo Chem Co Ltd | 熱可塑性樹脂変性ノボラック樹脂組成物及びその製造方法 |
| JP3915045B2 (ja) | 1997-03-31 | 2007-05-16 | フドー株式会社 | マシニングセンタにおける構造部品成形材料、及びマシニングセンタにおける構造部品成形体 |
| JP2000169669A (ja) | 1998-12-07 | 2000-06-20 | Zexel Corp | コンプレッサ―用部材及びその製造方法並びにスクロ―ルコンプレッサ― |
| JP2002129005A (ja) * | 2000-10-30 | 2002-05-09 | Sumitomo Bakelite Co Ltd | ポリエーテル芳香族ケトン系樹脂組成物並びにフィルム及びシート |
| JP2005281364A (ja) | 2004-03-29 | 2005-10-13 | Sumitomo Bakelite Co Ltd | フェノール樹脂成形材料 |
| WO2009031243A1 (ja) * | 2007-09-08 | 2009-03-12 | Toho Tenax Co., Ltd. | 繊維強化プリプレグ及びそれから得られる複合材料 |
| JP2011068778A (ja) * | 2009-09-25 | 2011-04-07 | Yokohama Rubber Co Ltd:The | 熱硬化性樹脂組成物 |
| JP2011099094A (ja) * | 2009-10-05 | 2011-05-19 | Yokohama Rubber Co Ltd:The | 繊維強化複合材料用エポキシ樹脂組成物、これを用いるプリプレグおよびハニカムサンドイッチパネル |
| JP2011213991A (ja) * | 2010-03-16 | 2011-10-27 | Toray Ind Inc | 炭素繊維強化複合材料 |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP2716708A4 |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2014237300A (ja) * | 2013-06-10 | 2014-12-18 | 三菱重工業株式会社 | 樹脂構造体並びに該樹脂構造体を含む樹脂製スクロール流体機械 |
| US11285221B2 (en) | 2014-06-16 | 2022-03-29 | Mayo Foundation For Medical Education And Research | Treating myelomas |
Also Published As
| Publication number | Publication date |
|---|---|
| EP2716708A1 (en) | 2014-04-09 |
| TW201311795A (zh) | 2013-03-16 |
| KR20140034840A (ko) | 2014-03-20 |
| EP2716708A4 (en) | 2015-05-27 |
| JP5715884B2 (ja) | 2015-05-13 |
| JP2012246450A (ja) | 2012-12-13 |
| CA2837681A1 (en) | 2012-12-06 |
| US20140107281A1 (en) | 2014-04-17 |
| CN103562307A (zh) | 2014-02-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP5715884B2 (ja) | スクロール成形品 | |
| US9862823B2 (en) | Resin composition for wet friction material, phenolic resin for wet friction material and wet friction material | |
| US10259902B2 (en) | Resol phenolic resin for friction material, method for producing the same, adhesive for friction material, and wet friction plate | |
| JP5780309B2 (ja) | 成形材料 | |
| JP2011042767A (ja) | ゴム補強用樹脂組成物 | |
| JP2012251131A (ja) | 成形材料 | |
| JP2008222897A (ja) | 摩擦材用フェノール樹脂組成物 | |
| JP2008189749A (ja) | 湿式ペーパー摩擦材用フェノール樹脂及び湿式ペーパー摩擦材 | |
| JP2011202075A (ja) | フェノール樹脂成形材料 | |
| JP2023167998A (ja) | レゾール型フェノール樹脂、フェノール樹脂組成物、およびレゾール型フェノール樹脂の製造方法 | |
| CN103282407B (zh) | 液态甲阶型酚醛树脂 | |
| JP5703660B2 (ja) | フェノール樹脂組成物の製造方法 | |
| JP2012067209A (ja) | フェノール樹脂組成物およびその製造方法並びに摩擦材 | |
| JP2011241269A (ja) | 界面強化処理ガラスフィラー及びフェノール樹脂成形材料 | |
| JP5023625B2 (ja) | 液状フェノール樹脂組成物 | |
| JP2008063440A (ja) | フェノール樹脂組成物 | |
| JP5644471B2 (ja) | フェノール樹脂成形材料の製造方法 | |
| JP2009179775A (ja) | フェノール樹脂組成物及び摩擦材 | |
| JP2010235671A (ja) | フェノール樹脂組成物 | |
| JPWO2012014807A1 (ja) | 液状フェノール樹脂およびその製造方法 | |
| JP2021004270A (ja) | フェノール樹脂 | |
| JP2009227817A (ja) | フェノール樹脂組成物およびその製造方法並びに摩擦材 | |
| JP5601191B2 (ja) | 摩擦材用フェノール樹脂組成物、変性フェノール樹脂の製造方法及び摩擦材 | |
| JP2021187918A (ja) | 湿式摩擦材用フェノール樹脂組成物、ならびに湿式摩擦材およびその製造方法 | |
| JP2009035662A (ja) | 摩擦材用フェノール樹脂組成物 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 12792347 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2837681 Country of ref document: CA |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 14123364 Country of ref document: US |
|
| ENP | Entry into the national phase |
Ref document number: 20137033759 Country of ref document: KR Kind code of ref document: A |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2012792347 Country of ref document: EP |