WO2015115394A1 - 耐食性溶射皮膜、その形成方法およびその形成用溶射装置 - Google Patents
耐食性溶射皮膜、その形成方法およびその形成用溶射装置 Download PDFInfo
- Publication number
- WO2015115394A1 WO2015115394A1 PCT/JP2015/052111 JP2015052111W WO2015115394A1 WO 2015115394 A1 WO2015115394 A1 WO 2015115394A1 JP 2015052111 W JP2015052111 W JP 2015052111W WO 2015115394 A1 WO2015115394 A1 WO 2015115394A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- corrosion
- flame
- resistant
- forming
- sprayed coating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C09—DYES; PAINTS; POLISHES; NATURAL RESINS; ADHESIVES; COMPOSITIONS NOT OTHERWISE PROVIDED FOR; APPLICATIONS OF MATERIALS NOT OTHERWISE PROVIDED FOR
- C09D—COATING COMPOSITIONS, e.g. PAINTS, VARNISHES OR LACQUERS; FILLING PASTES; CHEMICAL PAINT OR INK REMOVERS; INKS; CORRECTING FLUIDS; WOODSTAINS; PASTES OR SOLIDS FOR COLOURING OR PRINTING; USE OF MATERIALS THEREFOR
- C09D5/00—Coating compositions, e.g. paints, varnishes or lacquers, characterised by their physical nature or the effects produced; Filling pastes
- C09D5/08—Anti-corrosive paints
- C09D5/10—Anti-corrosive paints containing metal dust
- C09D5/103—Anti-corrosive paints containing metal dust containing Al
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B7/00—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas
- B05B7/16—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed
- B05B7/1606—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed the spraying of the material involving the use of an atomising fluid, e.g. air
- B05B7/1613—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed the spraying of the material involving the use of an atomising fluid, e.g. air comprising means for heating the atomising fluid before mixing with the material to be sprayed
- B05B7/162—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed the spraying of the material involving the use of an atomising fluid, e.g. air comprising means for heating the atomising fluid before mixing with the material to be sprayed and heat being transferred from the atomising fluid to the material to be sprayed
- B05B7/1626—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed the spraying of the material involving the use of an atomising fluid, e.g. air comprising means for heating the atomising fluid before mixing with the material to be sprayed and heat being transferred from the atomising fluid to the material to be sprayed at the moment of mixing
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B7/00—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas
- B05B7/16—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed
- B05B7/20—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed by flame or combustion
- B05B7/201—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed by flame or combustion downstream of the nozzle
- B05B7/203—Spraying apparatus for discharge of liquids or other fluent materials from two or more sources, e.g. of liquid and air, of powder and gas incorporating means for heating or cooling the material to be sprayed by flame or combustion downstream of the nozzle the material to be sprayed having originally the shape of a wire, rod or the like
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/01—Layered products comprising a layer of metal all layers being exclusively metallic
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B15/00—Layered products comprising a layer of metal
- B32B15/01—Layered products comprising a layer of metal all layers being exclusively metallic
- B32B15/012—Layered products comprising a layer of metal all layers being exclusively metallic one layer being formed of an iron alloy or steel, another layer being formed of aluminium or an aluminium alloy
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C21/00—Alloys based on aluminium
- C22C21/06—Alloys based on aluminium with magnesium as the next major constituent
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/04—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge characterised by the coating material
- C23C4/06—Metallic material
- C23C4/08—Metallic material containing only metal elements
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/12—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge characterised by the method of spraying
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/12—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge characterised by the method of spraying
- C23C4/129—Flame spraying
Definitions
- the present invention relates to a thermal spray coating that coats the surface of a structure or the like and a method and apparatus for forming the thermal spray coating, and in particular, to provide a thermal spray coating excellent in corrosion resistance against seawater, salt, and the like.
- the thermal spray material has a structure in which the fine particles are flattened when flying in the thermal spray stream and laminated on the substrate, and each fine particle is sprayed when heated and melted. Since it is oxidized by the air in the atmosphere, an oxide film is always generated on the surface, which causes a minute void to be formed through the oxide film, and the void serves as an internal infiltration path for an aqueous solution such as seawater. Yes.
- the cooling rate is not sufficient, so the crystal grain size of the Al-Mg structure in the formed film is as large as several tens of micrometers, and corrosion progresses from the grain boundary. Easy to do.
- Mg is easily oxidized in a flame, so the Mg concentration in the Al-Mg coating is lowered, and the predetermined corrosion resistance may not be exhibited. The decrease in Mg concentration may decrease the strength of the Al-Mg alloy film and worsen the scratch resistance.
- the present invention solves the above-described problems, and provides a corrosion-resistant film that exhibits an anticorrosion performance higher than that in a salt water environment and the like, and a method and apparatus for forming the same.
- the method of forming a corrosion-resistant sprayed coating according to the invention is: -A flame containing molten material particles is jetted toward the base material, and in the upstream region of the injection path (that is, the region in which the material particles are melted), the flame is separated from the outside air, and the downstream region (above In the front part following the upstream region), a spray gun having a function of forcibly cooling the material particles and the flame with a jet gas or a jet mist before reaching the base material is used.
- a corrosion-resistant alloy film is formed on the surface of the base material by using the above-mentioned material particles as a corrosion-resistant alloy containing Al (with an equivalent component ratio).
- the sprayed coating excellent in anticorrosion performance can be formed on the base-material surface, and a base material can fully be protected. Because a) In the upstream region of the injection path for injecting the flame containing the molten material particles toward the base material, that is, the region in which the material particles are melted, the flame and the outside air are separated from each other. Therefore, the corrosion resistance of the sprayed coating is not lowered, and cracks and partial red rust do not occur at an early stage. Accordingly, pores (holes) peculiar to the thermal spray coating can be reduced, and internal intrusion of seawater or the like serving as a corrosive medium can be effectively prevented.
- the corrosion-resistant alloy containing Al can be made into a microstructure (structure with a crystal grain size of 10 ⁇ m or less), and extremely high corrosion resistance can be imparted to the corrosion-resistant alloy film.
- the reason for using Al-containing material is that Al is a base metal compared to steel and can be expected to have excellent anticorrosion properties, Al is a naturally existing and harmless material, and Al It is lighter than steel.
- a corrosion-resistant sprayed coating may be formed on the surface of a substrate made of Al or Al alloy by the above method.
- the above-mentioned method of forming a corrosion-resistant sprayed coating can be applied to the surface of a steel structure such as a bridge or tower tank as a base material, but it is also used on the surface of a base material made of Al or Al alloy. be able to. This is because, as described above, the material particles and the flame are cooled by the jet gas or jet mist before reaching the base material, so that the temperature of the surface of the base material to be sprayed does not rise to the extent that the base material melts. .
- the base material made of Al or Al alloy can be appropriately coated and protected.
- the amount of oxygen supplied to the flame should be less than the amount of oxygen required for complete combustion. By doing so, oxidation of the molten material particles can be more effectively prevented, and the anticorrosion performance of the sprayed coating can be further improved.
- a material containing 0.3 to 15% by mass of Mg and the balance being made of Al is preferably used. Any of those containing Mg, Si, Mn, Ti, Cu and Al is preferably used.
- Mg is a base metal rather than the commonly used Zn, sacrificial anti-corrosion effect is more effective than the potential difference between steel and steel. Therefore, an effect that a dense protective film can be formed by containing Mg is obtained.
- the above-mentioned corrosion-resistant alloy material containing Al may be supplied to the above-mentioned spray gun in the state of a powder (mixture or alloy powder according to elements) or a wire (integrated as an alloy).
- a powder mixture or alloy powder according to elements
- a wire integrated as an alloy
- the apparatus for forming a corrosion-resistant sprayed coating according to the invention is: A thermal spraying apparatus for forming a corrosion-resistant alloy film containing Al on a substrate surface, ⁇ A flame containing molten material particles is injected toward the base material, and in the upstream region of the injection path, the flame and outside air are separated, and in the downstream region, the material particles and the flame reach the base material. It includes a thermal spray gun having a function of forcibly cooling with jet gas or jet mist from the front. According to such a forming apparatus, the above-described method for forming a corrosion-resistant sprayed coating is carried out to suppress the oxidation of material particles and the crystal grain size thereof is reduced. A corrosion resistant thermal spray coating can be formed on the substrate surface.
- -Corrosion-resistant alloy material is supplied in powder or wire (especially when supplied in the state of wire is advantageous in terms of cost, etc.)
- the above-mentioned jet gas or jet mist is supplied so as to form a cylindrical surface flow that becomes gradually thinner (thereby, the function of separating the flame from the outside air also in the downstream region of the flame injection path).
- the jet gas or jet mist is a concentric jet with the flame to be injected, and is inclined so that it intersects at a position on the flame center line, 3 to 7 times the width or diameter of the flame from the flame injection port.
- the amount of oxygen supplied to the flame in the upstream region is less than the amount of oxygen required for complete combustion (this effectively prevents the oxidation of the molten material particles),
- the molten material particles are cooled at a rate of 1 million ° C. or more per second by the jet gas or jet mist (thus making the crystal grain size particularly fine).
- the corrosion resistant alloy sprayed coating according to the invention is a coating formed by spraying, Contains Al, ⁇ Porosity is 1% or less, -It is characterized by having a microstructure with a crystal grain size of 10 ⁇ m or less (it is preferable that a so-called nanostructure with a crystal grain size of submicron is included in part).
- Such a corrosion-resistant alloy sprayed coating functions as an advantageous coating for corrosion protection for the following reasons. a) Since Al is a base metal compared to steel, it exhibits excellent corrosion resistance. Al is a naturally occurring and harmless material, and Al is also preferred in that it is lighter than steel.
- Porosity is 1% or less, and there are very few pores peculiar to the sprayed coating, and therefore internal intrusion of seawater or the like as a corrosive medium is effectively prevented.
- the following are also preferable. That is, -Containing 0.3 to 15% by mass of Mg, with the balance being Al. -Containing Mg, Si, Mn, Ti, Cu and Al. -It contains Mg and the total content of Mg and Al oxides is 0.2 mass% or less. ⁇ The film surface is covered with silicon or epoxy resin and sealed. In particular, if the total content of Mg and Al oxides is 0.2% by mass or less as described above, there is no deterioration in the anticorrosion performance due to the oxides, and there is no reduction in the strength of the film. It is also advantageous in that it has high adhesion.
- the above corrosion-resistant alloy film may be formed by thermal spraying on the substrate surface by the above-described forming method.
- the method or apparatus for forming a corrosion-resistant sprayed coating according to the invention can form a sprayed coating excellent in anticorrosive performance on the substrate surface. Moreover, the corrosion-resistant alloy sprayed coating according to the present invention exhibits superior anticorrosion performance compared to the prior art, for example, in a salt water environment.
- FIG. It is a side view which shows the hot wire type film forming apparatus 1 It is an assembly enlarged view which shows the front-end
- FIG. It is a result of a combined cycle test. It is a result of a polarization measurement test. It is SEM sectional drawing of the sample which sprayed Al-Mg on the iron base material. It is a ferroxyl test result. It is an EBSP analysis figure. It is a metal-microscope sectional view of the sample which sprayed Al-Mg on the Al base material. It is a side view which shows the powder type film forming apparatus.
- a corrosion-resistant alloy sprayed coating is formed on a surface of a steel structure, a steel plate or the like by using a material mainly composed of Al-Mg and spraying with a coating forming apparatus which is a special spray gun.
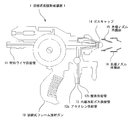
- the used hot wire film forming apparatus 1 is shown in FIGS.
- the illustrated hot-wire-type film forming apparatus 1 includes a double nozzle comprising a front-end nozzle inner cylinder 15 and a front-end nozzle outer cylinder 16 at the front end of a frame-type spray gun 10 that supplies a material for forming a film with a wire. Is attached as a means for external cooling, from which jet gas (or mist) for externally cooling the flame or the like is emitted.
- the flame-type flame spray gun 10 has a material wire supply pipe 11 for supplying a material wire to be sprayed by a gas turbine (for example, one using nitrogen), an acetylene supply pipe 12a and an oxygen supply pipe as fuel. 12b and an internal cooling gas (for example, nitrogen) supply pipe 13 are connected.
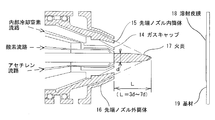
- a gas cap 14 is provided at the front end of the hot-wire flame spray gun 10, from which a flame 17 and a molten material (the material wire is melted) are injected as shown in FIG. 2.
- the internal cooling gas is blown out from a position in contact with the inside of the gas cap 14 to cool the gas cap 14 and adjust the temperature of the flame 17.
- a gas cap 14 is fixed to the hot wire frame spray gun 10 near the front end thereof by, for example, screwing with a tip nozzle inner cylinder 15, and the tip nozzle outer cylinder 16 is fixed to the tip nozzle inner cylinder 15. It is attached to the hot wire frame spray gun 10 via
- Jet gas (or jet mist) for external cooling is supplied to the conical surface-like gap between the tip nozzle inner cylinder 15 and the tip nozzle outer cylinder 16, and the flame 17 is provided from the annular nozzle at the tip. It is ejected toward the front center line. From these points, the film forming apparatus 1 including the tip nozzle outer cylinder 16 and the like a) supply a corrosion-resistant alloy material with a wire, b) gradually from the outer peripheral portion of the tip nozzle toward the front (downstream side) central portion.
- the tip nozzle outer cylinder 16 shown in FIG. 1 blows out a jet gas (for example, nitrogen) or a jet mist (for example, water mist) as described above, whereby a flame 17 (see FIG. 2) is sprayed by the hot wire type flame spray gun 10. ), That is, in the melting region where the material wire is melted, the flame 17 can be separated from the outside air.
- a double nozzle made of stainless steel is used, and as described above, the tip nozzle inner cylinder 15 and the tip nozzle outer cylinder 16 are concentrically arranged to provide a gap therebetween, and the gap is formed by jet gas or jet mist. It is used as a flow path and as a spout for the same gas.
- the cooling gas flows between the double nozzles (the tip nozzle inner cylinder 15 and the tip nozzle outer cylinder 16), the temperature rise of the tip nozzle inner cylinder 15 and the like is suppressed.
- the gap between the double nozzles (tip nozzle inner cylinder 15 and tip nozzle outer cylinder 16) is provided toward the center line of the flame 17, and the jet gas or jet mist positively jets toward the center of the flame 17. It is supposed to be. Since the intersection of the jet gas or jet mist and the center line of the flame 17 is positioned forward from the jet port of the flame 17 by a distance 3 to 7 times the diameter of the flame 17, the jet gas or jet mist Has a function of quenching a sufficiently melted material at the tip of the flame 17 to refine its structure.
- the thermal spray coating 18 can be formed on the surface of the substrate 19 as shown on the right side of FIG. Since the flame 17 injected from the gas cap 14 of the hot wire flame spray gun 10 reaches the base material 19 surrounded by the jet gas or jet mist jetted by the tip nozzle outer cylinder 16 (the jet port), The amount of oxide present in the thermal spray coating 18 is small. Moreover, since it is rapidly cooled as described above, the crystal grain size of the thermal spray coating 18 is fine.
- a film forming apparatus 2 shown in FIG. 9 may be used.
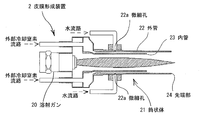
- the film forming apparatus 2 has a cylindrical body 21 or the like attached to the front portion of the powder-type flame spray gun 20 that can also be called an external cooling device.
- a carrier gas for example, nitrogen
- a supply tube for acetylene and oxygen as fuel for example, and an internal cooling gas (for example, nitrogen)
- an internal cooling gas for example, nitrogen
- the cylindrical body 21 separates the flame from the outside air in the first half of the flame sprayed by the spray gun 20, that is, the melting region where the material powder is melted, and the jet mist or jet gas from the tip to the second half of the flame (front). It is for spewing out.
- a stainless steel double circular tube is used as the cylindrical body 21, and the outer tube 22 and the inner tube 23 are arranged concentrically to provide a gap therebetween.
- a jet mist or jet gas for externally cooling the flame and the molten material is supplied to the gap and ejected from the tip portion 24.
- a good Al-Mg film having excellent corrosion resistance can be formed on the surface of a steel structure. it can. Also, a good film can be formed on the surface of a base material made of Al or an Al alloy instead of a steel structure. This is because when the forming apparatus 1 or 2 is used, the molten material and the flame are cooled by the jet gas or the jet mist, so that the thermal influence on the substrate is small.
- Film formation by thermal spraying was performed by the following procedure. First, the surface of the steel plate (base material) is blasted with an alumina grid or a steel grid. Next, the Al—Mg material is sprayed onto the surface of the base material by the film forming apparatus 1 (melting wire type) or 2 (powder type). That is, the Al-Mg material is melted in a reducing atmosphere by adjusting the ratio of acetylene and oxygen, which are combustion gases, and by flowing a jet gas or jet mist along a double nozzle, A thermal spray coating is formed on the steel sheet (base material) with a cooling rate of about 1 million ° C. or more per second. Note that, unless otherwise noted, thermal spraying was performed under the conditions of Examples 1 to 3 as the present invention, and thermal spraying was performed under the conditions of Comparative Examples 1 and 2 as the prior art. Each condition is shown in Table 1.
- Example 1 and Comparative Example 1 were evaluated by conducting a corrosion acceleration test in which a cycle consisting of [° C./humidity 25% ⁇ 4 hours) ⁇ wet (high temperature) (50 ° C./humidity 98% ⁇ 2 hours) was repeated. In this test, the thickness of the sprayed coating on the test piece was 150 to 200 ⁇ m.
- Example 1 The white rust in Comparative Example 1 is an oxide of Al or Mg, suggesting that the coating deteriorates early. In Example 1, red rust or white rust even after 1,000 hours (125 cycles) has elapsed. It was good with no occurrence.
- CASS test Copper Accelerated Acetic Acid Salt Spray Test
- the spray test was carried out for 48 hours at 2 / h and compressed air pressure of 0.098 MPa.
- Example 1 and Comparative Example 1 were evaluated.
- the film thickness of the test piece was 250 to 300 ⁇ m.
- Table 2 below shows changes in surface condition and weight changes such as discoloration, stains, corrosion, surface deterioration, and peeling of the test pieces after the test.
- Al (OH) 3 corrosion products are produced by the dissolution reaction of Al, and the weight of the gel Al (OH) 3 is reduced by flowing down.
- Elemental analysis test Table 3 shows the analysis results obtained by ICP emission spectroscopy and inert gas melting method. From Table 3, there is no difference in the proportion of oxygen in the thermal spray material between Example 1 and Comparative Example 1, but in the thermal spray coating, Example 1 has an oxygen content of 0.2% by mass or less. It is 2% by mass or more. Therefore, it can be said that Example 1 can prevent oxidation of Al and Mg as compared with Comparative Example 1.
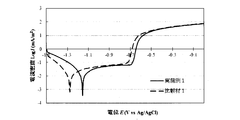
- Example 1 Electrochemical measurement test Polarization measurement was performed on each film of Example 1 and Comparative Example 1, and the results are shown in FIG.
- the natural potential of Example 1 was ⁇ 1.161V, and the natural potential of Comparative Example 1 was ⁇ 1.277V.
- the Al-Mg coating is less basic than steel and performs sacrificial protection.
- the natural potential of steel is ⁇ 0.4V to ⁇ 0.6V.
- Example 1 is more noble than Comparative Example 1, and since the anticorrosion current is suppressed from Comparative Example 1, the diffusion of oxygen in the Al-Mg sprayed coating is suppressed, and the anticorrosion life in salt water is improved. I can expect.
- Example 5 SEM images SEM observation was performed on Examples 1 to 3 and Comparative Example 1, and the SEM images are shown in FIG. In Examples 1 to 3, the porosity is 1% or less, and it can be confirmed that there are few pores and cracks compared to Comparative Example 1.
- pure water was added to 10 g of potassium hexacyanoferrate trihydrate, 10 g of potassium hexacyanoferrate, and 60 g of sodium chloride to prepare 1,000 ml, and a ferroxyl test was conducted in Example 1. If there is a defect reaching the substrate, blue spots can be observed, but Example 1 has no spots. The ferroxyl test results of Example 1 are shown in FIG.
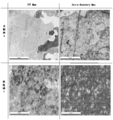
- Example 1 EBSP analysis EBSP analysis (electron backscattering pattern) was performed on the films of Example 1 and Comparative Example 2, and the results are shown in FIG.
- the crystal grain size of Example 1 is 10 ⁇ m or less, and it can be confirmed that the grain size is very fine compared to Comparative Example 2.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Organic Chemistry (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Mechanical Engineering (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Physics & Mathematics (AREA)
- Plasma & Fusion (AREA)
- Combustion & Propulsion (AREA)
- Wood Science & Technology (AREA)
- Life Sciences & Earth Sciences (AREA)
- Coating By Spraying Or Casting (AREA)
- Nozzles (AREA)
- Laminated Bodies (AREA)
Abstract
【課題】 塩水環境等において従来以上の防食性能を発揮する耐食性皮膜やその形成方法・形成装置を提供するものである。 【解決手段】 a)溶融した材料粒子を含む火炎を基材に向けて噴射し、当該噴射経路の上流側(すなわち材料粒子を溶融させる)領域では火炎と外気とを隔てる機能を有するとともに、下流側領域(上記上流側領域に続く部分)では上記材料粒子および火炎を基材に達する前から噴流ガスまたは噴流ミストによって強制冷却する機能を有する溶射ガンを用い、b)Alを含有する耐食性合金材料を上記材料粒子とすることにより、基材表面上に耐食性合金皮膜を形成する。
Description
本発明は、構造物等の表面を被覆する溶射皮膜やその形成方法・形成装置に関し、特に海水や塩分等に対する耐食性に優れた溶射皮膜を提供するためのものである。
海洋気象地域に構築されている鋼構造物は、海水や海塩粒子による腐食によって著しく損耗することが知られている。そのため、これらの鋼構造物には何らかの防食表面処理を施して腐食を抑制する工夫が払われている。その代表的なものとして、塗装処理や溶融亜鉛めっき処理、溶融アルミニウムめっき処理がある。
その他の方法では、溶射法によって、電気化学的に卑な電位を示す亜鉛やアルミニウムまたはそれらの合金類の溶射皮膜を形成する方法もある。しかし鋼構造物に施される亜鉛やアルミニウムなどの金属溶射皮膜による従来の防食技術は、ある程度の防食作用は認められるものの、犠牲陽極作用によって鋼構造物を保護するものであるため定期的な再溶射が必要である(下記の特許文献1・2を参照)。
そこで、亜鉛やアルミニウムよりも塩水環境における良好な特性を付与することができる耐食性合金、例えばAl-Mg合金が溶射されることも近年では多くなった。
その他の方法では、溶射法によって、電気化学的に卑な電位を示す亜鉛やアルミニウムまたはそれらの合金類の溶射皮膜を形成する方法もある。しかし鋼構造物に施される亜鉛やアルミニウムなどの金属溶射皮膜による従来の防食技術は、ある程度の防食作用は認められるものの、犠牲陽極作用によって鋼構造物を保護するものであるため定期的な再溶射が必要である(下記の特許文献1・2を参照)。
そこで、亜鉛やアルミニウムよりも塩水環境における良好な特性を付与することができる耐食性合金、例えばAl-Mg合金が溶射されることも近年では多くなった。
しかし、溶射皮膜の場合、多孔質となるため塩害の影響を受けやすく、鋼構造物の腐食損耗速度が大きいという問題がある。更に、一般的な溶射皮膜において溶射材料はその微粒子が溶射気流中を飛行する際に扁平化されて基材上に積層した構造を呈すると共に、それぞれの微粒子は、加熱、溶融される際に溶射雰囲気中の空気によって酸化されるため、その表面には必ず酸化膜が生成し、酸化膜を介することで微小な空隙を生成する原因となり、その空隙が海水などの水溶液の内部浸入経路となっている。
このような原因で、従来、Al-Mg溶射による防食法であっても、皮膜の耐用年数は、海岸部のような厳しい塩水環境の場所では数十年程度にすぎない。今後の日本における人口減少を伴うインフラ整備環境を考えると、それ以上、たとえば百年程度保つことが強く望まれるところである。
このような原因で、従来、Al-Mg溶射による防食法であっても、皮膜の耐用年数は、海岸部のような厳しい塩水環境の場所では数十年程度にすぎない。今後の日本における人口減少を伴うインフラ整備環境を考えると、それ以上、たとえば百年程度保つことが強く望まれるところである。
Al-Mgを通常のフレーム溶射ガンで溶射した場合、冷却速度が十分でないため、形成される皮膜中のAl-Mg組織の結晶粒径が数10μmと大きく、結晶粒界を基点に腐食が進展し易い。また通常のフレーム溶射ガンで溶射した場合、Mgが火炎中で酸化され易いため、Al-Mg皮膜中のMg濃度が下がり、所定の防食性が発揮されないことがある。Mg濃度の減少はAl-Mg合金皮膜の強度を低下させ耐傷付き性を悪化させることもある。Al溶射皮膜は犠牲防食作用がZnに比べて劣るため、溶射時に僅かな割れが入ることにより、早期に部分的に赤錆が発生し、外観及び性能を損なう欠点がある。また通常のフレーム溶射ガンで溶射時の酸化によって形成されたMg酸化物もしくはAl酸化物は、防食性を低下させる。
本発明は、上記の課題を解決するものであり、塩水環境等において従来以上の防食性能を発揮する耐食性皮膜やその形成方法・形成装置を提供するものである。
発明による耐食性溶射皮膜の形成方法は、
・ 溶融した材料粒子を含む火炎を基材に向けて噴射し、当該噴射経路の上流側領域(すなわち材料粒子を溶融させる領域)では火炎と外気とを隔てる機能を有するとともに、下流側領域(上記上流側領域に続く前方の部分)では上記材料粒子および火炎を基材に達する前から噴流ガスまたは噴流ミストによって強制冷却する機能を有する溶射ガンを用い、
・ Alを含有する耐食性合金(と同等の成分比率の)材料を上記材料粒子とすることにより、基材表面上に耐食性合金皮膜を形成することを特徴とする。
基材または材料の種類等によっては、上記のガンで溶射を開始する前に基材を予熱するのがよい場合もある。
・ 溶融した材料粒子を含む火炎を基材に向けて噴射し、当該噴射経路の上流側領域(すなわち材料粒子を溶融させる領域)では火炎と外気とを隔てる機能を有するとともに、下流側領域(上記上流側領域に続く前方の部分)では上記材料粒子および火炎を基材に達する前から噴流ガスまたは噴流ミストによって強制冷却する機能を有する溶射ガンを用い、
・ Alを含有する耐食性合金(と同等の成分比率の)材料を上記材料粒子とすることにより、基材表面上に耐食性合金皮膜を形成することを特徴とする。
基材または材料の種類等によっては、上記のガンで溶射を開始する前に基材を予熱するのがよい場合もある。
上記の形成方法によれば、防食性能に優れた溶射皮膜を基材表面上に形成し、基材を十分に保護することができる。なぜなら、
a) 溶融した材料粒子を含む火炎を基材に向けて噴射するその噴射経路の上流側領域、すなわち材料粒子を溶融させる領域において、火炎と外気とが隔てられるため、溶融した上記材料粒子が酸化しがたく、したがって溶射皮膜の防食性が低下せず、また割れが入ったり早期に部分的な赤錆が発生したりすることがない。それにともなって、溶射皮膜特有の気孔(空孔)を少なくすることができ、腐食媒体となる海水などの内部浸入を効果的に防止することができる。
b) 下流側領域において、上記材料粒子および火炎を、それが基材に達する前から噴流ガスまたは噴流ミストによって強制冷却するため、毎秒100万℃程度かそれ以上のきわめて高い速度で材料粒子を冷却することができる。そのため、Alを含有する耐食性合金をミクロ組織(結晶粒径が10μm以下の組織)とすることができ、当該耐食性合金皮膜にきわめて高い耐食性を付与することができる。
なお、Alを含有する材料を素材とする理由は、Alが鋼に比べて卑な金属であり優れた防食性が期待できること、Alは自然に存在し無害な材料であること、また、Alが鋼に比べて軽量であることである。
a) 溶融した材料粒子を含む火炎を基材に向けて噴射するその噴射経路の上流側領域、すなわち材料粒子を溶融させる領域において、火炎と外気とが隔てられるため、溶融した上記材料粒子が酸化しがたく、したがって溶射皮膜の防食性が低下せず、また割れが入ったり早期に部分的な赤錆が発生したりすることがない。それにともなって、溶射皮膜特有の気孔(空孔)を少なくすることができ、腐食媒体となる海水などの内部浸入を効果的に防止することができる。
b) 下流側領域において、上記材料粒子および火炎を、それが基材に達する前から噴流ガスまたは噴流ミストによって強制冷却するため、毎秒100万℃程度かそれ以上のきわめて高い速度で材料粒子を冷却することができる。そのため、Alを含有する耐食性合金をミクロ組織(結晶粒径が10μm以下の組織)とすることができ、当該耐食性合金皮膜にきわめて高い耐食性を付与することができる。
なお、Alを含有する材料を素材とする理由は、Alが鋼に比べて卑な金属であり優れた防食性が期待できること、Alは自然に存在し無害な材料であること、また、Alが鋼に比べて軽量であることである。
上記方法によって耐食性溶射皮膜を、AlまたはAl合金でできた基材の表面上に形成するのもよい。
上記した耐食性溶射皮膜の形成方法は、橋梁や塔槽類などの鋼構造物を基材としてその表面に適用することができるが、AlまたはAl合金等でできた基材の表面にも使用することができる。上記のとおり噴流ガスまたは噴流ミストによって、基材に達する前から材料粒子および火炎を冷却するため、溶射対象となる基材の表面が、基材が溶融する程度までには温度上昇しないからである。そうしてAlまたはAl合金製の基材表面に上記皮膜を形成することにより、AlまたはAl合金製の基材を適切に被覆し保護することができる。
上記した耐食性溶射皮膜の形成方法は、橋梁や塔槽類などの鋼構造物を基材としてその表面に適用することができるが、AlまたはAl合金等でできた基材の表面にも使用することができる。上記のとおり噴流ガスまたは噴流ミストによって、基材に達する前から材料粒子および火炎を冷却するため、溶射対象となる基材の表面が、基材が溶融する程度までには温度上昇しないからである。そうしてAlまたはAl合金製の基材表面に上記皮膜を形成することにより、AlまたはAl合金製の基材を適切に被覆し保護することができる。
火炎と外気とが隔てられる上記の上流側領域においては、火炎に供給される酸素の量を完全燃焼に必要な酸素量よりも少なくするのがよい。
そのようにすると、溶融した上記材料粒子の酸化がさらに効果的に防止され、溶射皮膜の防食性能を一層向上させることができる。
そのようにすると、溶融した上記材料粒子の酸化がさらに効果的に防止され、溶射皮膜の防食性能を一層向上させることができる。
上記の耐食性合金材料として、
・ Mgを0.3~15質量%含有し、残部がAlよりなるもの
・ Mg、Si、Mn、Ti、CuおよびAlを含有するもの
のいずれかを使用すると好ましい。
AlとともにMgを含有する素材を使用すると、表面硬度を向上できることに加え、Mgは一般に用いられるZnより卑な金属であるため、鋼を基材とするときの鋼との電位差より犠牲防食効果が大きく、したがってMgの含有によって緻密な保護皮膜が生成できるといった効果が得られる。
なお、発明による形成方法や形成装置(後述)によれば、Alを含有しない上記以外の材料を溶射することも可能であり、それによって、ミクロ組織を有していて耐食性能等に優れた各種の金属皮膜を基材上に形成することが可能である。
・ Mgを0.3~15質量%含有し、残部がAlよりなるもの
・ Mg、Si、Mn、Ti、CuおよびAlを含有するもの
のいずれかを使用すると好ましい。
AlとともにMgを含有する素材を使用すると、表面硬度を向上できることに加え、Mgは一般に用いられるZnより卑な金属であるため、鋼を基材とするときの鋼との電位差より犠牲防食効果が大きく、したがってMgの含有によって緻密な保護皮膜が生成できるといった効果が得られる。
なお、発明による形成方法や形成装置(後述)によれば、Alを含有しない上記以外の材料を溶射することも可能であり、それによって、ミクロ組織を有していて耐食性能等に優れた各種の金属皮膜を基材上に形成することが可能である。
Alを含有する上記の耐食性合金材料は、粉末(元素別の混合物もしくは合金粉末)またはワイヤ(合金として一体にされたもの)の状態で上記の溶射ガンに供給するとよい。
とくに、ワイヤの状態で供給できると、皮膜の原料コスト面と現場作業面で有利であるうえ、材料の取扱いが容易である点でも有利である。
とくに、ワイヤの状態で供給できると、皮膜の原料コスト面と現場作業面で有利であるうえ、材料の取扱いが容易である点でも有利である。
発明による耐食性溶射皮膜の形成装置は、
・ Alを含有する耐食性合金皮膜を基材表面上に形成するための溶射装置であって、
・ 溶融した材料粒子を含む火炎を基材に向けて噴射し、当該噴射経路の上流側領域では火炎と外気とを隔てる機能を有するとともに、下流側領域では上記材料粒子および火炎を基材に達する前から噴流ガスまたは噴流ミストによって強制冷却する機能を有する溶射ガンを含むことを特徴とする。
こうした形成装置によれば、上記した耐食性溶射皮膜の形成方法を実施して、材料粒子の酸化が抑制されるとともにその結晶粒径が小さくされた、気孔が少なくて防食性能の高い、Al含有の耐食性溶射皮膜を基材表面上に形成することができる。
・ Alを含有する耐食性合金皮膜を基材表面上に形成するための溶射装置であって、
・ 溶融した材料粒子を含む火炎を基材に向けて噴射し、当該噴射経路の上流側領域では火炎と外気とを隔てる機能を有するとともに、下流側領域では上記材料粒子および火炎を基材に達する前から噴流ガスまたは噴流ミストによって強制冷却する機能を有する溶射ガンを含むことを特徴とする。
こうした形成装置によれば、上記した耐食性溶射皮膜の形成方法を実施して、材料粒子の酸化が抑制されるとともにその結晶粒径が小さくされた、気孔が少なくて防食性能の高い、Al含有の耐食性溶射皮膜を基材表面上に形成することができる。
上記の形成装置に関しては、以下のいずれか(または全部)の特徴がともなっているとさらに好ましい。すなわち、
・ 耐食性合金材料が粉末またはワイヤで供給されること(とくにワイヤの状態で供給されると、コスト等の面で有利である)、
・ 上記の噴流ガスまたは噴流ミストが、次第に細くなる筒形面状の流れをなすように供給されること(それによって、火炎の噴射経路の下流側領域においても、火炎と外気とを隔てる機能が冷却機能と併せて発揮される)、
・ 噴流ガスまたは噴流ミストは、噴射する火炎と同心円状の噴流とされ、火炎噴射口から火炎の幅または直径の3~7倍だけ前方の、火炎中心線上の位置で交わるように、傾斜を付けて供給されること(そうすると、噴流ガスまたは噴流ミストが火炎と強く接触し、火炎の冷却速度を高めるとともに結晶粒子を微細化することができる)、
・ 上流側領域で火炎に供給される酸素の量が、完全燃焼に必要な酸素量よりも少ないこと(そうすると、溶融した材料粒子の酸化がとくに効果的に防止される)、
・ 噴流ガスまたは噴流ミストによって、溶融した上記材料の粒子が毎秒100万℃以上の速度で冷却されること(それにより、結晶粒径がとくに微細になる)。
・ 耐食性合金材料が粉末またはワイヤで供給されること(とくにワイヤの状態で供給されると、コスト等の面で有利である)、
・ 上記の噴流ガスまたは噴流ミストが、次第に細くなる筒形面状の流れをなすように供給されること(それによって、火炎の噴射経路の下流側領域においても、火炎と外気とを隔てる機能が冷却機能と併せて発揮される)、
・ 噴流ガスまたは噴流ミストは、噴射する火炎と同心円状の噴流とされ、火炎噴射口から火炎の幅または直径の3~7倍だけ前方の、火炎中心線上の位置で交わるように、傾斜を付けて供給されること(そうすると、噴流ガスまたは噴流ミストが火炎と強く接触し、火炎の冷却速度を高めるとともに結晶粒子を微細化することができる)、
・ 上流側領域で火炎に供給される酸素の量が、完全燃焼に必要な酸素量よりも少ないこと(そうすると、溶融した材料粒子の酸化がとくに効果的に防止される)、
・ 噴流ガスまたは噴流ミストによって、溶融した上記材料の粒子が毎秒100万℃以上の速度で冷却されること(それにより、結晶粒径がとくに微細になる)。
発明による耐食性合金溶射皮膜は、溶射によって形成された皮膜であり、
・ Alを含有し、
・ 気孔率が1%以下であるとともに、
・ 結晶粒径が10μm以下のミクロ組織をなしている(結晶粒径がサブミクロンという、いわゆるナノ組織を一部に含んでいるのも好ましい)ことを特徴とする。
このような耐食性合金溶射皮膜は、以下のような理由により、防食のための有利な皮膜として機能する。
a) Alは、鋼に比べて卑な金属であるために、優れた防食性を発揮する。Alは自然に存在し無害な材料であり、またAlが鋼に比べて軽量であるという点でも好ましい。
b) 気孔率が1%以下であって溶射皮膜特有の気孔がきわめて少なく、したがって、腐食媒体となる海水などの内部浸入が効果的に防止される。
c) 結晶粒径が10μm以下というミクロ組織をなしているため、通常のフレーム溶射ガンでAl合金を溶射することにより形成された従来の皮膜とは違って、結晶粒界を基点に腐食が進展する現象が生じにくい。
・ Alを含有し、
・ 気孔率が1%以下であるとともに、
・ 結晶粒径が10μm以下のミクロ組織をなしている(結晶粒径がサブミクロンという、いわゆるナノ組織を一部に含んでいるのも好ましい)ことを特徴とする。
このような耐食性合金溶射皮膜は、以下のような理由により、防食のための有利な皮膜として機能する。
a) Alは、鋼に比べて卑な金属であるために、優れた防食性を発揮する。Alは自然に存在し無害な材料であり、またAlが鋼に比べて軽量であるという点でも好ましい。
b) 気孔率が1%以下であって溶射皮膜特有の気孔がきわめて少なく、したがって、腐食媒体となる海水などの内部浸入が効果的に防止される。
c) 結晶粒径が10μm以下というミクロ組織をなしているため、通常のフレーム溶射ガンでAl合金を溶射することにより形成された従来の皮膜とは違って、結晶粒界を基点に腐食が進展する現象が生じにくい。
上記の耐食性溶射皮膜については、以下のものも好ましい。すなわち、
・ Mgを0.3~15質量%含有し、残部がAlよりなるもの。
・ Mg、Si、Mn、Ti、CuおよびAlを含有するもの。
・ Mgを含有するとともに、MgおよびAlの酸化物の合計含有量が0.2質量%以下であるもの。
・ 皮膜表面が、シリコンまたはエポキシ樹脂で被覆され封孔されているもの。
とくに、上記のようにMgおよびAlの酸化物の合計含有量が0.2質量%以下であると、当該酸化物による防食性能の低下が見られないうえ、皮膜の強度低下がないので、耐傷付き性が高い点でも有利である。
また、皮膜表面が、シリコンまたはエポキシ樹脂で被覆されることにより封孔されていると、僅かに気孔が存在するとしてもそれが封じられるため、海水などの浸入が防止され防食性能が低下しない。
以上のような耐食性合金皮膜は、前述の形成方法にて基材表面上に溶射することにより形成するとよい。
・ Mgを0.3~15質量%含有し、残部がAlよりなるもの。
・ Mg、Si、Mn、Ti、CuおよびAlを含有するもの。
・ Mgを含有するとともに、MgおよびAlの酸化物の合計含有量が0.2質量%以下であるもの。
・ 皮膜表面が、シリコンまたはエポキシ樹脂で被覆され封孔されているもの。
とくに、上記のようにMgおよびAlの酸化物の合計含有量が0.2質量%以下であると、当該酸化物による防食性能の低下が見られないうえ、皮膜の強度低下がないので、耐傷付き性が高い点でも有利である。
また、皮膜表面が、シリコンまたはエポキシ樹脂で被覆されることにより封孔されていると、僅かに気孔が存在するとしてもそれが封じられるため、海水などの浸入が防止され防食性能が低下しない。
以上のような耐食性合金皮膜は、前述の形成方法にて基材表面上に溶射することにより形成するとよい。
発明による耐食性溶射皮膜の形成方法または形成装置は、防食性能に優れた溶射皮膜を基材表面上に形成することができる。また、発明による耐食性合金溶射皮膜は、たとえば塩水環境等において、従来以上の優れた防食性能を発揮する。
以下、本発明について詳細に説明する。鋼構造物や鋼板等の表面に、Al-Mgを主体とする材料を用い、特殊溶射ガンである皮膜形成装置にて溶射することにより耐食性合金溶射皮膜を形成する。
使用した溶線式皮膜形成装置1を図1および図2に示す。
図示の溶線式皮膜形成装置1は、皮膜とするための材料をワイヤで供給するフレーム式溶射ガン10の先端部に、先端ノズル内筒体15と先端ノズル外筒体16とからなる二重ノズルを外部冷却用の手段として取り付け、それより、火炎等を外部冷却するための噴流ガス(またはミスト)を出すようにしたものである。
図示の溶線式皮膜形成装置1は、皮膜とするための材料をワイヤで供給するフレーム式溶射ガン10の先端部に、先端ノズル内筒体15と先端ノズル外筒体16とからなる二重ノズルを外部冷却用の手段として取り付け、それより、火炎等を外部冷却するための噴流ガス(またはミスト)を出すようにしたものである。
溶線式フレーム溶射ガン10は、図示は省略したが、溶射する材料ワイヤをガス式タービン(たとえば窒素を用いるもの)により供給する材料ワイヤ供給管11と、燃料とするアセチレン供給管12aおよび酸素供給管12b、ならびに内部冷却ガス(たとえば窒素)の供給管13とが接続されている。溶線式フレーム溶射ガン10の前端にはガスキャップ14があり、それより図2のように火炎17と溶融材料(上記材料ワイヤが溶融したもの)とを噴射する。上記の内部冷却ガスは、ガスキャップ14の内側に接する位置から吹き出してガスキャップ14の冷却と火炎17の温度調節をする。溶線式フレーム溶射ガン10には、その前端付近で、ガスキャップ14を先端ノズル内筒体15にて、例えば螺合して固定し、先端ノズル外筒体16は、そうした先端ノズル内筒体15を介して溶線式フレーム溶射ガン10に取り付けている。
先端ノズル内筒体15と先端ノズル外筒体16との間の円錐面状の隙間には、外部冷却のための噴流ガス(または噴流ミスト)が供給され、先端の環状の噴流口より火炎17の前方中心線上へ向けて噴出させられる。こうした点から、先端ノズル外筒体16等を含む皮膜形成装置1は、a)耐食性合金材料をワイヤで供給する、b)先端ノズルの外周部から前方(下流側)中央部へ向けて、次第に細くなる筒形面状の流れをなすように、溶融した上記材料粒子と火炎とを冷却する上記の噴流ガスまたは噴流ミストを供給する、c)噴流ガスまたは噴流ミストを、噴射する火炎と同心円状(横断面において火炎の外側で火炎と同心円をなす形状)に噴流し、火炎噴射口から、火炎の直径に対し3~7倍の火炎の距離の中心線上で交わるように傾斜を付けて供給する――といった特徴的な機能をなす。
図1に示す先端ノズル外筒体16は、上記のように噴流ガス(たとえば窒素)または噴流ミスト(たとえば水ミスト)を吹き出すことにより、溶線式フレーム溶射ガン10が噴射する火炎17(図2参照)の前半部分、すなわち材料ワイヤを溶融させる溶融領域において火炎17と外気とを隔てることができる。この例ではステンレス製の二重ノズルとし、上記のとおり先端ノズル内筒体15と先端ノズル外筒体16とを同心に配置して両者間に隙間を設け、その隙間を噴流ガスまたは噴流ミストの流路にするとともに同ガス等の噴流口としている。二重ノズル(先端ノズル内筒体15と先端ノズル外筒体16)の間に冷却ガスを流すので先端ノズル内筒体15等の温度上昇が抑制される。二重ノズル(先端ノズル内筒体15と先端ノズル外筒体16)の隙間は火炎17の中心線に向かって設けられており、噴流ガスまたは噴流ミストは積極的に火炎17の中心に向かい噴流するようになっている。噴流ガスまたは噴流ミストと火炎17の中心線との交点は、火炎17の噴射口から火炎17の直径の3~7倍の距離だけ前方に位置するようになっているため、噴流ガスまたは噴流ミストは、十分に溶融した材料を火炎17の先端部分で急冷し、その組織を微細化する作用がある。
図1の溶線式皮膜形成装置1を使用するとき、図2の右方に示すように基材19の表面に溶射皮膜18を形成することができる。溶線式フレーム溶射ガン10のガスキャップ14から噴射される火炎17は、先端ノズル外筒体16(上記の噴流口)により噴流される噴流ガスまたは噴流ミストに囲まれて基材19に達するため、溶射皮膜18中に介在する酸化物の量が少ない。また、上記のとおり急冷されるために溶射皮膜18の結晶粒径は微細である。
図1・図2に示す皮膜形成装置1の代わりに、図9に示す皮膜形成装置2を使用してもよい。皮膜形成装置2は、粉体式フレーム溶射ガン20の前部に、外部冷却装置ともいえる筒状体21等を取り付けたものである。溶射ガン20の本体の図示は省略したが、溶射する材料粉末を搬送ガス(たとえば窒素)とともに供給するする管と、燃料とするアセチレンおよび酸素の各供給管、ならびに内部冷却ガス(たとえば窒素)の供給管とが接続されている。溶射ガン20から火炎と溶融材料(上記粉末の溶融したもの)とを噴射する。
筒状体21は、溶射ガン20が噴射する火炎の前半部分、すなわち材料粉末を溶融させる溶融領域において火炎と外気とを隔てるとともに、先端部より火炎の後半部(前方)に噴流ミストもしくは噴流ガスを噴き出すためのものである。この例では、筒状体21としてステンレス製の二重円管を使用し、外管22と内管23とを同心に配置して両者間に隙間を設けている。その隙間に、火炎と溶融材料とを外部冷却するための噴流ミストもしくは噴流ガスを供給し、先端部24より噴出させる。これに関し、外管22に開けた微細孔22aより水を滴下すると、窒素ガスのエジェクター効果により噴流ミストが形成され、外管22と内管23の隅間を噴流ミストが流れて先端部24より噴射される。
筒状体21は、溶射ガン20が噴射する火炎の前半部分、すなわち材料粉末を溶融させる溶融領域において火炎と外気とを隔てるとともに、先端部より火炎の後半部(前方)に噴流ミストもしくは噴流ガスを噴き出すためのものである。この例では、筒状体21としてステンレス製の二重円管を使用し、外管22と内管23とを同心に配置して両者間に隙間を設けている。その隙間に、火炎と溶融材料とを外部冷却するための噴流ミストもしくは噴流ガスを供給し、先端部24より噴出させる。これに関し、外管22に開けた微細孔22aより水を滴下すると、窒素ガスのエジェクター効果により噴流ミストが形成され、外管22と内管23の隅間を噴流ミストが流れて先端部24より噴射される。
図1・図2に示す皮膜形成装置1、または図9の皮膜形成装置2のいずれの装置を用いても、耐食性に優れた良好なAl-Mg皮膜を鋼構造物の表面に形成することができる。
また、鋼構造物ではなく、AlまたはAl合金等でできた基材の表面に対しても、同様に良好な皮膜を形成できる。形成装置1または2を用いると、噴流ガスまたは噴流ミストによって溶融材料および火炎が冷却されるため、基材への熱影響が小さいからである。
また、鋼構造物ではなく、AlまたはAl合金等でできた基材の表面に対しても、同様に良好な皮膜を形成できる。形成装置1または2を用いると、噴流ガスまたは噴流ミストによって溶融材料および火炎が冷却されるため、基材への熱影響が小さいからである。
溶射による皮膜形成を、つぎの手順により行った。
まず、鋼板(基材)に対し、アルミナグリッドもしくスチールグリッドにより表面をブラスト処理する。次に、皮膜形成装置1(溶線式)または2(粉末式)により、Al-Mg材料を基材表面に溶射する。すなわち、Al-Mg材料を、燃焼ガスであるアセチレンと酸素の比を調整して還元性雰囲気で溶融し、二重ノズルに沿って噴流ガスまたは噴流ミストを流すことで、溶融した材料と外気とを隔て、毎秒100万℃程度以上の冷却速度を伴い、鋼板(基材)に溶射皮膜を形成する。
なお、特に追記の無い場合、本発明としては実施例1~3の条件にて溶射を行い、従来技術としては比較例1、2の条件にて溶射した。各条件を表1に示す。
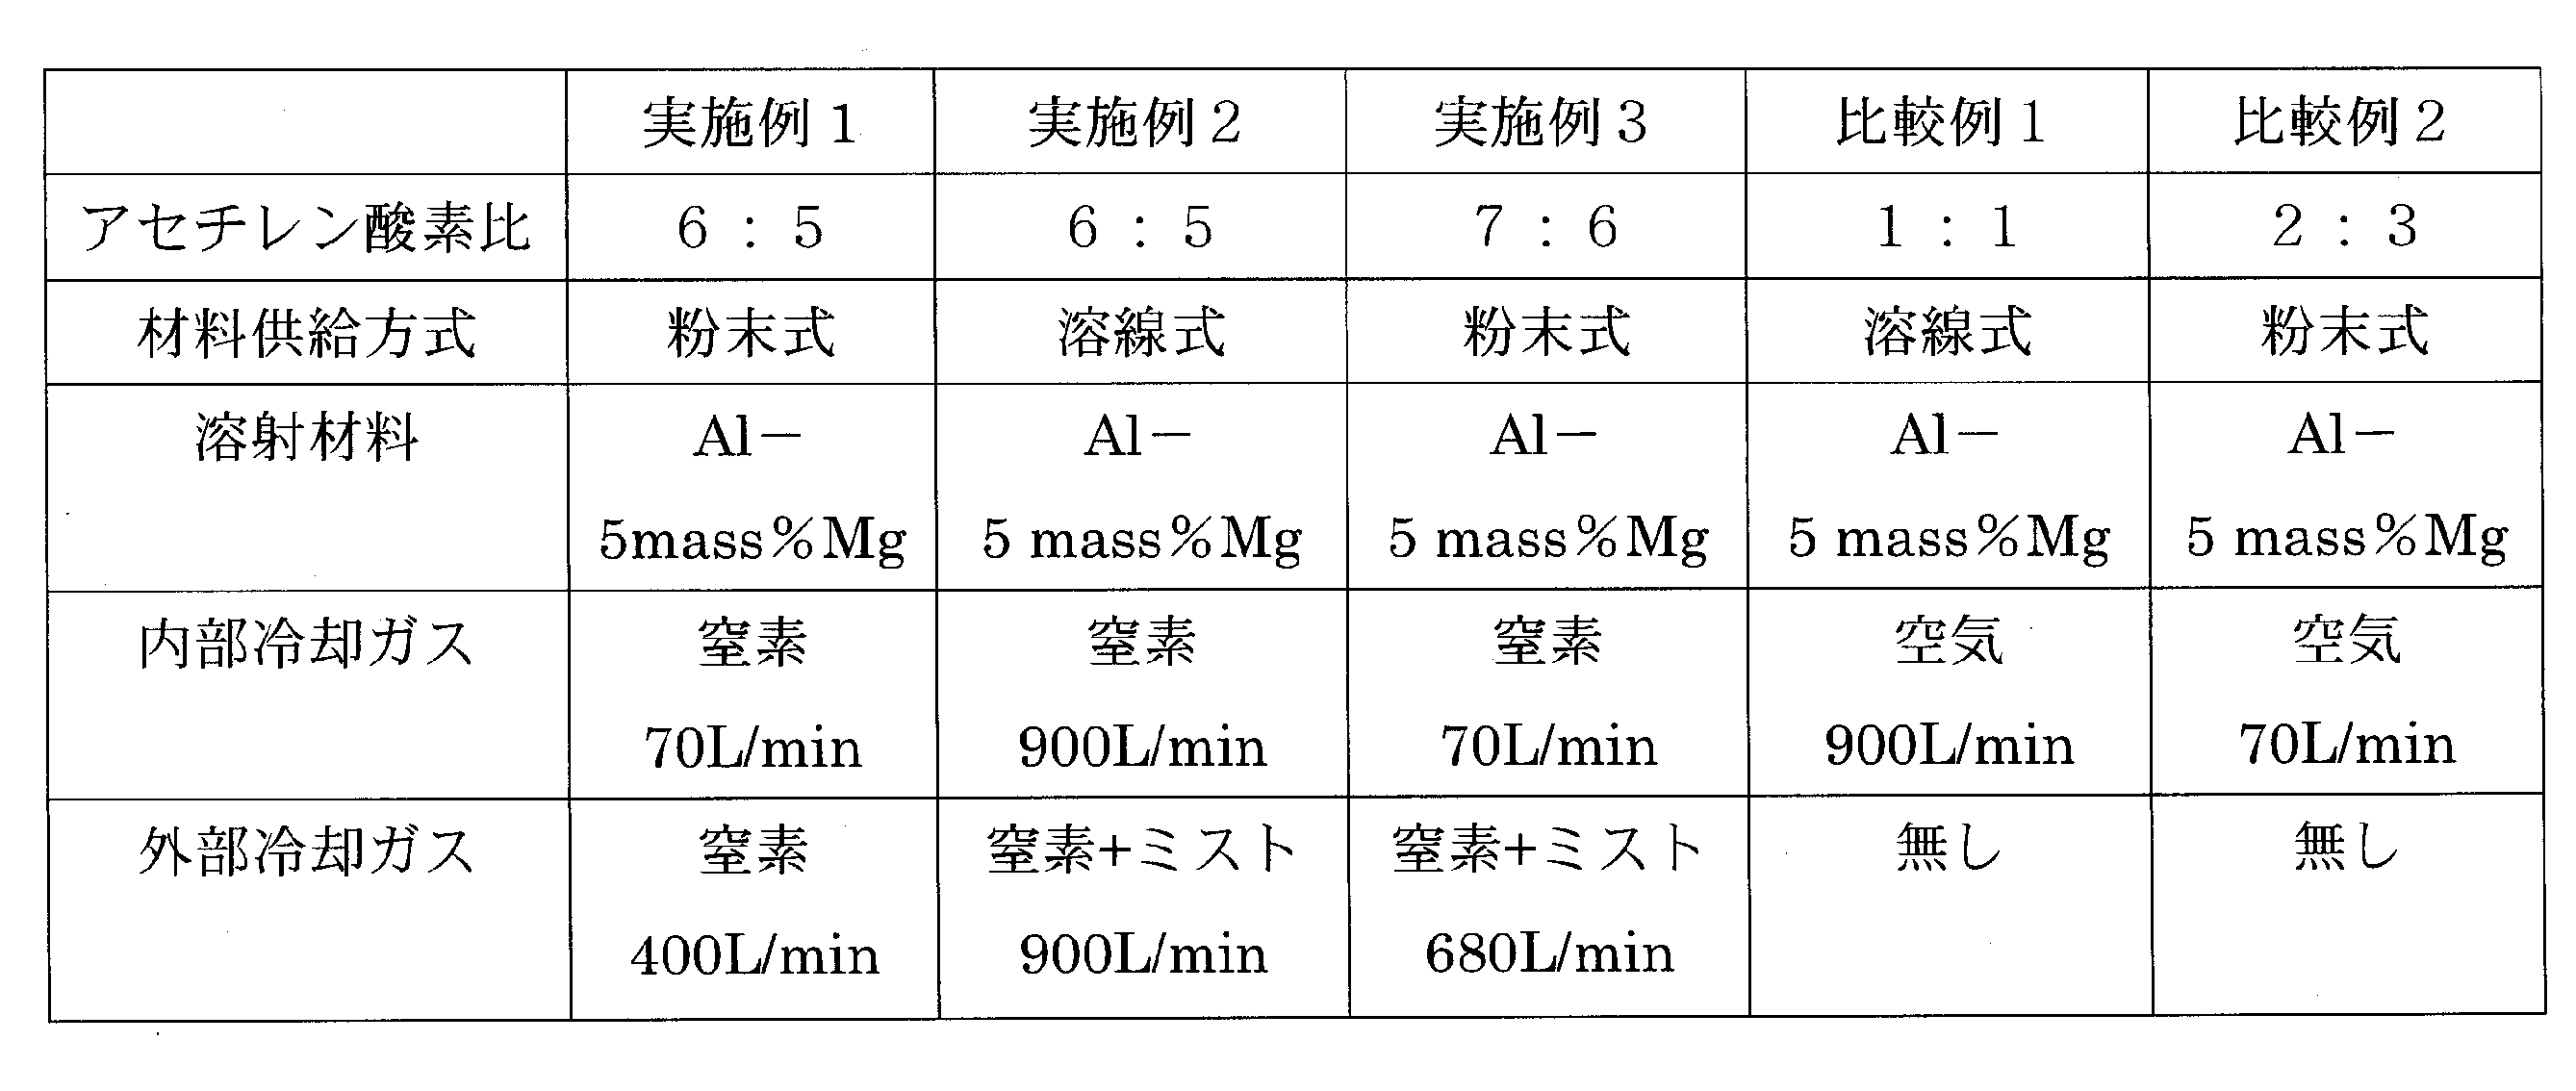
まず、鋼板(基材)に対し、アルミナグリッドもしくスチールグリッドにより表面をブラスト処理する。次に、皮膜形成装置1(溶線式)または2(粉末式)により、Al-Mg材料を基材表面に溶射する。すなわち、Al-Mg材料を、燃焼ガスであるアセチレンと酸素の比を調整して還元性雰囲気で溶融し、二重ノズルに沿って噴流ガスまたは噴流ミストを流すことで、溶融した材料と外気とを隔て、毎秒100万℃程度以上の冷却速度を伴い、鋼板(基材)に溶射皮膜を形成する。
なお、特に追記の無い場合、本発明としては実施例1~3の条件にて溶射を行い、従来技術としては比較例1、2の条件にて溶射した。各条件を表1に示す。
上記によって鋼板(基材)の表面に形成されたAl-Mg皮膜について、以下のように試験を行ってその性質を調べた。
1) 複合サイクル試験
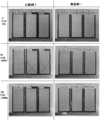
平板耐食性の評価は、溶射皮膜を設けた鋼板に対し、JASO M 609,610に準拠した塩水噴霧(5%NaCl水溶液・35℃・湿度100%・2時間)→乾燥(65℃・湿度25%・4時間)→湿潤(高温)(50℃・湿度98%・2時間)からなるサイクルを繰り返し与える腐食促進試験を行い、実施例1と比較例1を評価した。本試験では試験片における溶射皮膜の膜厚は150~200μmとした。なお、溶射皮膜を設けた鋼板には、カッターで、鋼素地に達する傷を入れたうえ、上記の試験を行った。試験後の皮膜の写真図3に示す。比較例1における白錆は、AlあるいはMgの酸化物であり、早期に皮膜が劣化することを示唆しており、実施例1では、1,000時間(125サイクル)経過後も赤錆あるいは白錆の発生はなく良好であった。
1) 複合サイクル試験
平板耐食性の評価は、溶射皮膜を設けた鋼板に対し、JASO M 609,610に準拠した塩水噴霧(5%NaCl水溶液・35℃・湿度100%・2時間)→乾燥(65℃・湿度25%・4時間)→湿潤(高温)(50℃・湿度98%・2時間)からなるサイクルを繰り返し与える腐食促進試験を行い、実施例1と比較例1を評価した。本試験では試験片における溶射皮膜の膜厚は150~200μmとした。なお、溶射皮膜を設けた鋼板には、カッターで、鋼素地に達する傷を入れたうえ、上記の試験を行った。試験後の皮膜の写真図3に示す。比較例1における白錆は、AlあるいはMgの酸化物であり、早期に皮膜が劣化することを示唆しており、実施例1では、1,000時間(125サイクル)経過後も赤錆あるいは白錆の発生はなく良好であった。
2) CASS試験(Copper Accelerated Acetic Acid Salt Spray Test)
JIS H 8502に準拠した、塩化ナトリウム40g/L 塩化第二銅0.205g/L pH3.0の試験液を、空気飽和器温度 63℃、試験槽温度 50℃、噴霧量 2.0 mL/80cm2/h、圧縮空気圧力 0.098MPaで、噴霧試験を48時間実施した。実施例1と比較例1を評価した。本試験では試験片の膜厚は250~300μmとした。試験後の試験片の変色、しみ、腐食、表面の劣化、剥離等、表面状態の変化と重量変化は下記の表2のようになった。Alの溶解反応によりAl(OH)3の腐食生成物ができ、ゲル状Al(OH)3が流れ落ちることで重量減少となる。
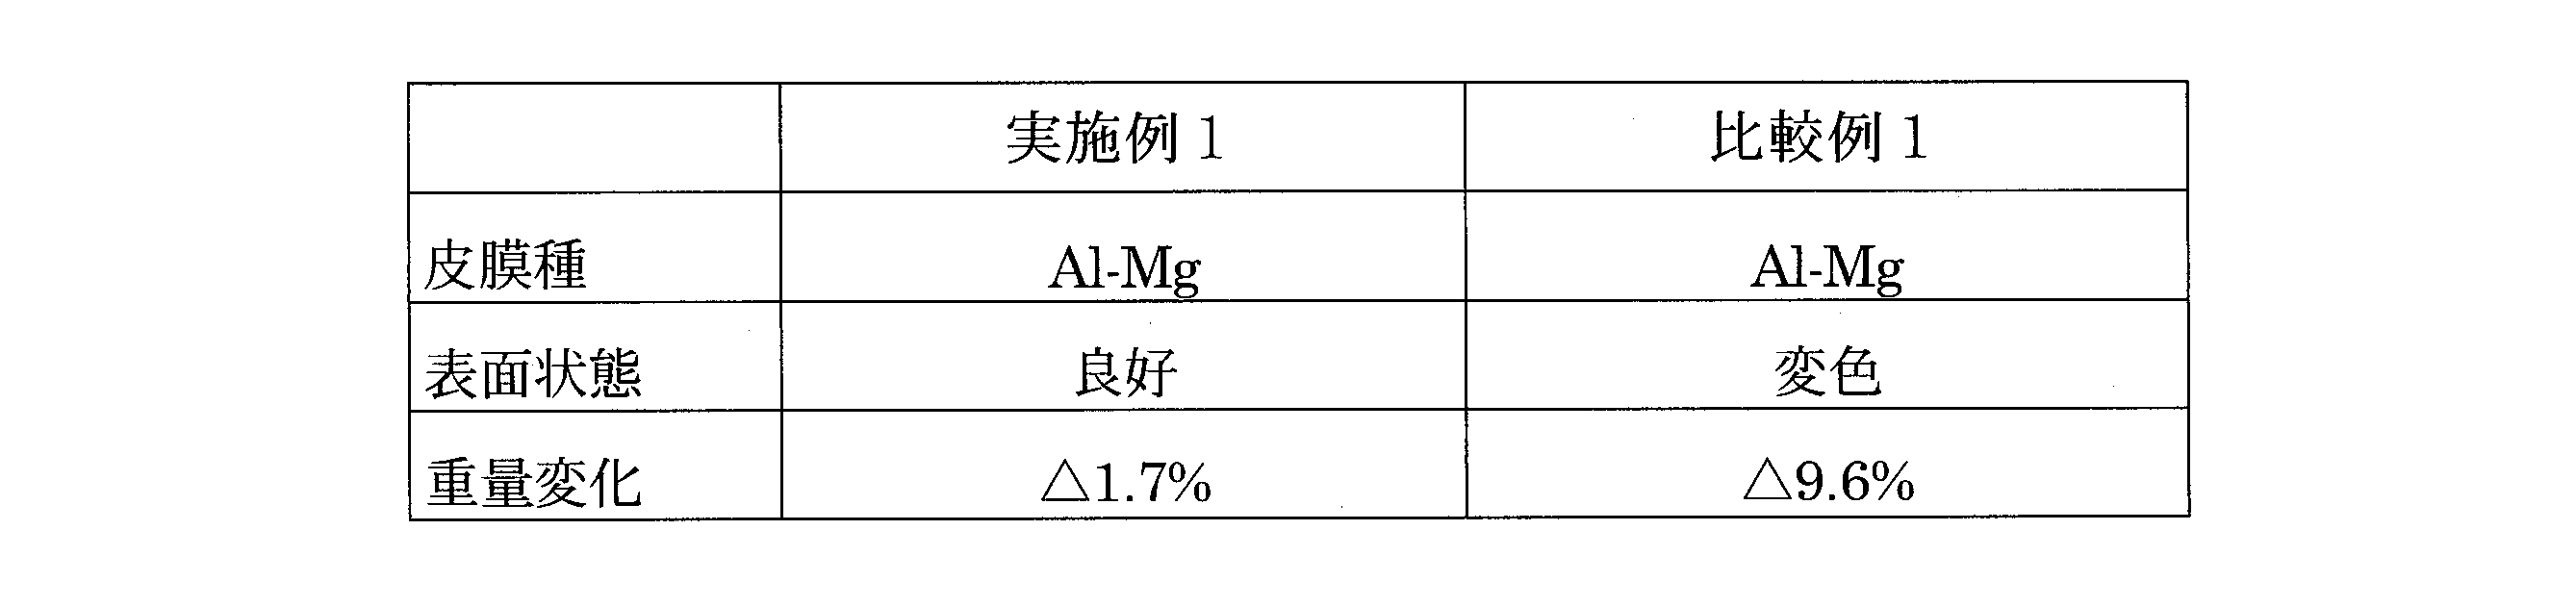
JIS H 8502に準拠した、塩化ナトリウム40g/L 塩化第二銅0.205g/L pH3.0の試験液を、空気飽和器温度 63℃、試験槽温度 50℃、噴霧量 2.0 mL/80cm2/h、圧縮空気圧力 0.098MPaで、噴霧試験を48時間実施した。実施例1と比較例1を評価した。本試験では試験片の膜厚は250~300μmとした。試験後の試験片の変色、しみ、腐食、表面の劣化、剥離等、表面状態の変化と重量変化は下記の表2のようになった。Alの溶解反応によりAl(OH)3の腐食生成物ができ、ゲル状Al(OH)3が流れ落ちることで重量減少となる。
3) 元素分析試験
ICP発光分光分析法および不活性ガス溶融法によって得られた分析結果を表3に示す。表3より、実施例1と比較例1では溶射材料の酸素の割合に差はないが、溶射皮膜では実施例1は酸素の含有量が0.2質量%以下であり比較例1では0.2質量%以上となっている。よって実施例1は比較例1と比べAlとMgの酸化が防止できているといえる。
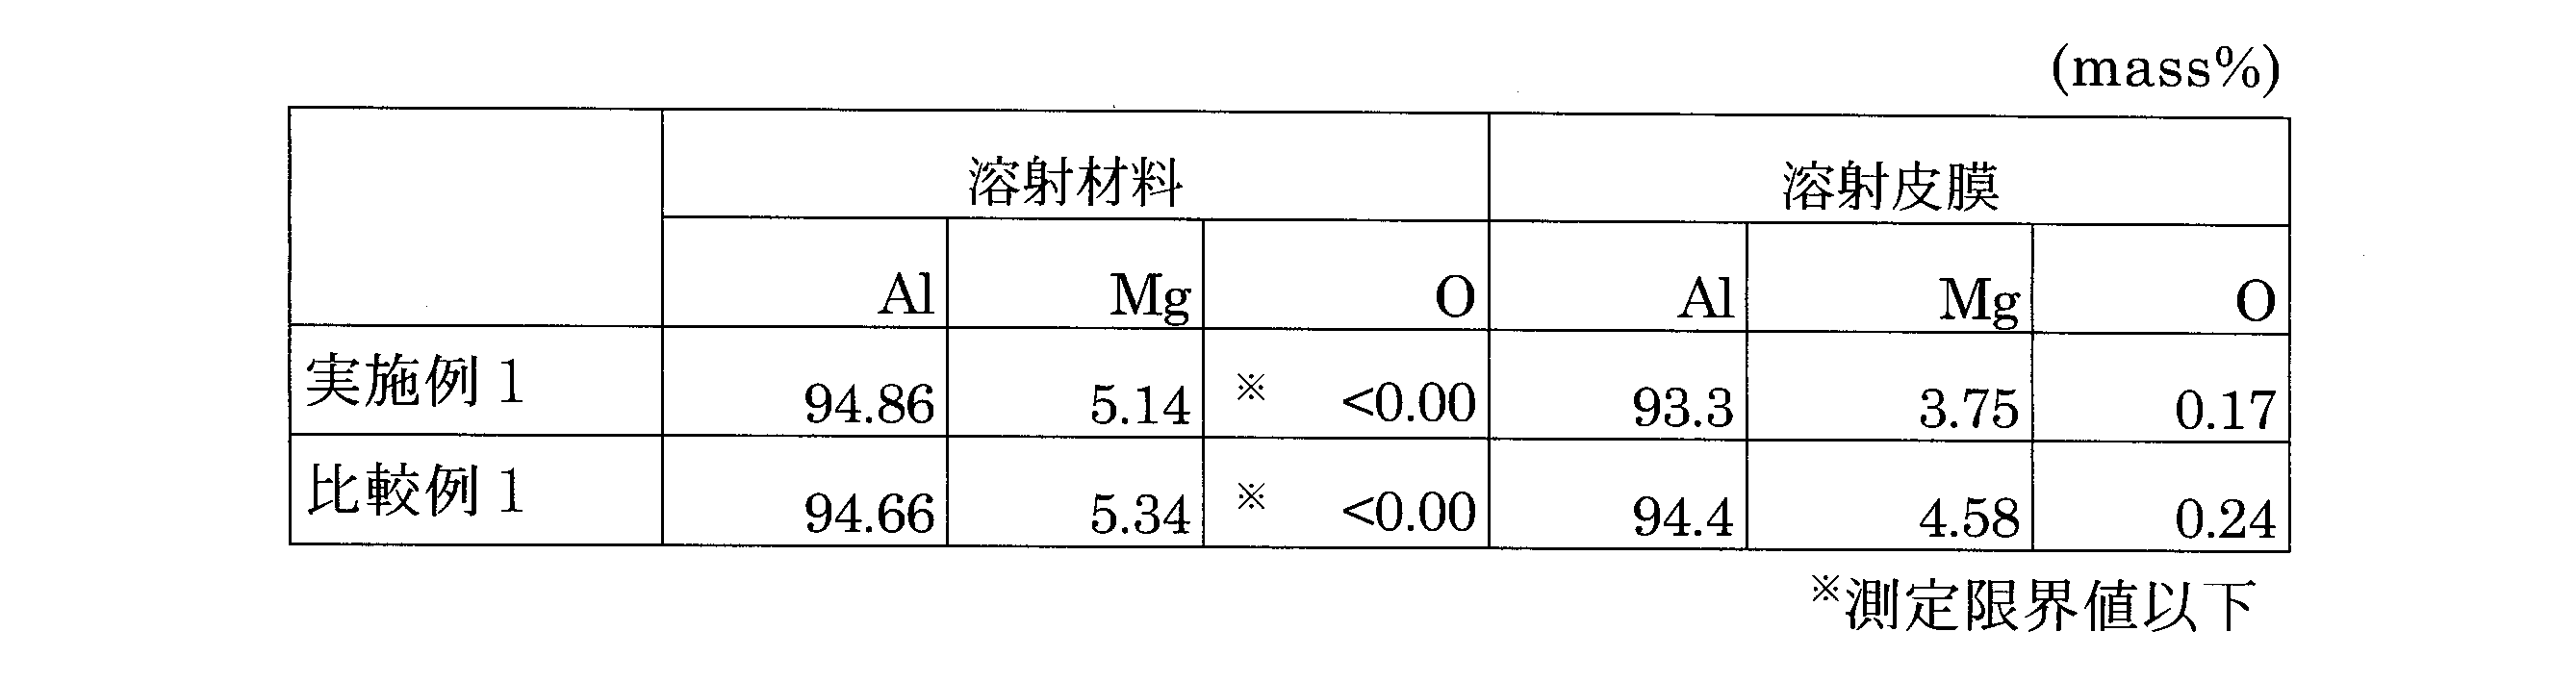
ICP発光分光分析法および不活性ガス溶融法によって得られた分析結果を表3に示す。表3より、実施例1と比較例1では溶射材料の酸素の割合に差はないが、溶射皮膜では実施例1は酸素の含有量が0.2質量%以下であり比較例1では0.2質量%以上となっている。よって実施例1は比較例1と比べAlとMgの酸化が防止できているといえる。
4) 電気化学測定試験
分極測定を実施例1と比較例1の各皮膜ついて行い、結果を図4に示す。実施例1の自然電位は△1.161V、比較例1の自然電位は△1.277Vであった。Al-Mg皮膜は鋼に比べて卑であって犠牲防食機能を果たす。なお鋼の自然電位は△0.4Vから△0.6V。実施例1は比較例1より貴であり、また、防食電流が比較例1より抑制されていることからAl-Mg溶射皮膜中の酸素の拡散が押さえられ、塩水中での防食寿命の向上が期待できる。
分極測定を実施例1と比較例1の各皮膜ついて行い、結果を図4に示す。実施例1の自然電位は△1.161V、比較例1の自然電位は△1.277Vであった。Al-Mg皮膜は鋼に比べて卑であって犠牲防食機能を果たす。なお鋼の自然電位は△0.4Vから△0.6V。実施例1は比較例1より貴であり、また、防食電流が比較例1より抑制されていることからAl-Mg溶射皮膜中の酸素の拡散が押さえられ、塩水中での防食寿命の向上が期待できる。
5) SEM画像
実施例1~3、比較例1に対しSEM観察を行い、SEM画像を図5に示す。実施例1~3は気孔率が1%以下であり比較例1と比較して気孔や割れの少ないことが確認できる。
なおJIS K 8617に従いヘキサシアノ鉄酸カリウム三水和物10g、ヘキサシアノ鉄酸カリウム10g、塩化ナトリウウム60gに純水を加え1,000mlを調整し、フェロキシル試験を実施例1に行った。基材まで達する欠陥があれば青い斑点を観察できるが、実施例1は斑点がない。実施例1のフェロキシル試験結果を図6に示す。
実施例1~3、比較例1に対しSEM観察を行い、SEM画像を図5に示す。実施例1~3は気孔率が1%以下であり比較例1と比較して気孔や割れの少ないことが確認できる。
なおJIS K 8617に従いヘキサシアノ鉄酸カリウム三水和物10g、ヘキサシアノ鉄酸カリウム10g、塩化ナトリウウム60gに純水を加え1,000mlを調整し、フェロキシル試験を実施例1に行った。基材まで達する欠陥があれば青い斑点を観察できるが、実施例1は斑点がない。実施例1のフェロキシル試験結果を図6に示す。
6) EBSP解析
EBSP解析(電子後方散乱パターン)を実施例1と比較例2の皮膜について行い、結果を図7に示す。実施例1のものは結晶粒径が10μm以下であり、比較例2と比較して粒径が非常に細かいことが確認できる。
EBSP解析(電子後方散乱パターン)を実施例1と比較例2の皮膜について行い、結果を図7に示す。実施例1のものは結晶粒径が10μm以下であり、比較例2と比較して粒径が非常に細かいことが確認できる。
図1・図2または図9の皮膜形成装置1・2を使用して溶射を行う場合、溶融した材料および火炎が噴流ガスまたは噴流ミストによる外部冷却によって急冷されるため、基材への熱影響は小さく、融点の低い基材(AlまたはAl合金等)であっても不都合がない。
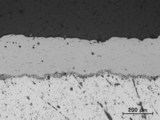
そこで、実施例1と同じ条件を使用するとともに基材をAlとし、当該基材の表面に溶射皮膜を形成した。その金属顕微鏡断面図を図8に示す。
そこで、実施例1と同じ条件を使用するとともに基材をAlとし、当該基材の表面に溶射皮膜を形成した。その金属顕微鏡断面図を図8に示す。
Claims (17)
- Alを含有し、気孔率が1%以下であるとともに結晶粒径が10μm以下のミクロ組織をなしていることを特徴とする耐食性合金溶射皮膜。
- Mgを0.3~15質量%含有し、残部がAlよりなることを特徴とする請求項1に記載の耐食性合金溶射皮膜。
- Mg、Si、Mn、Ti、CuおよびAlを含有することを特徴とする請求項1または2に記載の耐食性合金溶射皮膜。
- MgおよびAlの酸化物の合計含有量が0.2質量%以下であることを特徴とする請求項1~3のいずれかに記載の耐食性合金溶射皮膜。
- 溶融した材料粒子を含む火炎を基材に向けて噴射し、当該噴射経路の上流側領域では火炎と外気とを隔てる機能を有するとともに下流側領域では上記材料粒子および火炎を基材に達する前から噴流ガスまたは噴流ミストにより強制冷却する機能を有する溶射ガンを用いて、基材表面上に形成されたことを特徴とする請求項1~4のいずれかに記載の耐食性合金溶射皮膜。
- 皮膜表面が、シリコンまたはエポキシ樹脂で被覆されることにより封孔されていることを特徴とする請求項1~5のいずれかに記載の耐食性合金溶射皮膜。
- 溶融した材料粒子を含む火炎を基材に向けて噴射し、当該噴射経路の上流側領域では火炎と外気とを隔てる機能を有するとともに、下流側領域では上記材料粒子および火炎を基材に達する前から噴流ガスまたは噴流ミストによって強制冷却する機能を有する溶射ガンを用い、
Alを含有する耐食性合金材料を上記材料粒子とすることにより、基材表面上に耐食性合金皮膜を形成することを特徴とする耐食性溶射皮膜の形成方法。 - AlまたはAl合金でできた基材の表面上に耐食性合金皮膜を形成することを特徴とする請求項7に記載した耐食性皮膜の形成方法
- 火炎が外気と隔てられた上記の上流側領域で火炎に供給される酸素の量を、完全燃焼に必要な酸素量よりも少なくすることを特徴とする請求項7または8に記載した耐食性溶射皮膜の形成方法。
- 上記の耐食性合金材料として、Mgを0.3~15質量%含有し、残部がAlよりなるものを使用することを特徴とする請求項7~9のいずれかに記載した耐食性溶射皮膜の形成方法。
- 上記の耐食性合金材料として、Mg、Si、Mn、Ti、CuおよびAlを含有するものを使用することを特徴とする請求項7~10のいずれかに記載した耐食性溶射皮膜の形成方法。
- 上記の耐食性合金材料を、粉末またはワイヤの状態で上記の溶射ガンに供給することを特徴とする請求項7~11のいずれかに記載した耐食性溶射皮膜の形成方法。
- Alを含有する耐食性合金皮膜を基材表面上に形成するための溶射装置であって、
溶融した材料粒子を含む火炎を基材に向けて噴射し、当該噴射経路の上流側領域では火炎と外気とを隔てる機能を有するとともに、下流側領域では上記材料粒子および火炎を基材に達する前から噴流ガスまたは噴流ミストによって強制冷却する機能を有する溶射ガンを含むことを特徴とする耐食性溶射皮膜の形成装置。 - 先端ノズルの中央から、噴射する火炎と、Alを含有していて当該火炎で溶融させられる耐食性合金材料の粉末またはワイヤと、上記先端ノズルを冷却するガスとを供給し、
当該先端ノズルの外周部から前方中央部へ向けて、次第に細くなる筒形面状の流れをなすように、溶融した上記材料粒子と火炎とを冷却する上記の噴流ガスまたは噴流ミストを供給する
ことを特徴とする請求項13に記載した耐食性溶射皮膜の形成装置。 - 溶融した上記材料粒子と火炎とを冷却する上記の噴流ガスまたは噴流ミストを、噴射する火炎と同心円状の噴流とし、火炎噴出口から火炎の幅または直径の3~7倍の距離だけ前方の火炎中心線上で交わるように傾斜を付けて供給することを特徴とする請求項13または14に記載した耐食性溶射皮膜の形成装置。
- 火炎と外気とが隔てられた上記の上流側領域で火炎に供給される酸素の量が、完全燃焼に必要な酸素量よりも少ないことを特徴とする請求項13~15のいずれかに記載した耐食性溶射皮膜の形成装置。
- 上記の噴流ガスまたは噴流ミストによって、溶融した上記材料の粒子を毎秒100万℃以上の速度で冷却することを特徴とする請求項13~16のいずれかに記載した耐食性溶射皮膜の形成装置。
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201580006682.XA CN106062236A (zh) | 2014-01-31 | 2015-01-27 | 耐腐蚀性热喷涂涂层、其形成方法及其形成用热喷涂装置 |
| EP15742600.8A EP3101151B1 (en) | 2014-01-31 | 2015-01-27 | Corrosion-resistant sprayed coating and method for forming same |
| US15/115,746 US10323153B2 (en) | 2014-01-31 | 2015-01-27 | Corrosion-resistant sprayed coating, method for forming same and spraying device for forming same |
| ES15742600T ES2797741T3 (es) | 2014-01-31 | 2015-01-27 | Recubrimiento pulverizado resistente a la corrosión y método para formar el mismo |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2014017943A JP6367567B2 (ja) | 2014-01-31 | 2014-01-31 | 耐食性溶射皮膜、その形成方法およびその形成用溶射装置 |
| JP2014-017943 | 2014-01-31 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2015115394A1 true WO2015115394A1 (ja) | 2015-08-06 |
Family
ID=53756967
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2015/052111 Ceased WO2015115394A1 (ja) | 2014-01-31 | 2015-01-27 | 耐食性溶射皮膜、その形成方法およびその形成用溶射装置 |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US10323153B2 (ja) |
| EP (1) | EP3101151B1 (ja) |
| JP (1) | JP6367567B2 (ja) |
| CN (1) | CN106062236A (ja) |
| ES (1) | ES2797741T3 (ja) |
| WO (1) | WO2015115394A1 (ja) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2017122253A (ja) * | 2016-01-05 | 2017-07-13 | 吉川工業株式会社 | 金属溶射皮膜及びその作製方法 |
Families Citing this family (18)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP6367567B2 (ja) * | 2014-01-31 | 2018-08-01 | 吉川工業株式会社 | 耐食性溶射皮膜、その形成方法およびその形成用溶射装置 |
| JP2017008394A (ja) * | 2015-06-24 | 2017-01-12 | 有限会社エスエスシー | 低温溶射用hvaf溶射装置 |
| US10221654B2 (en) | 2015-08-26 | 2019-03-05 | Geodynamics, Inc. | Reverse flow arming and actuation apparatus and method |
| US10240446B2 (en) | 2015-08-26 | 2019-03-26 | Geodynamics, Inc. | Reverse flow seat forming apparatus and method |
| US10294752B2 (en) | 2015-08-26 | 2019-05-21 | Geodynamics, Inc. | Reverse flow catch-and-release tool and method |
| US9611721B2 (en) | 2015-08-26 | 2017-04-04 | Geodynamics, Inc. | Reverse flow sleeve actuation method |
| JP6924990B2 (ja) * | 2016-06-17 | 2021-08-25 | 吉川工業株式会社 | 溶射皮膜及び溶射皮膜部材 |
| JP2018141214A (ja) * | 2017-02-28 | 2018-09-13 | 吉川工業株式会社 | 耐水素脆性溶射皮膜及び耐水素脆性溶射皮膜部材 |
| CN111684109A (zh) | 2017-10-24 | 2020-09-18 | 臼井国际产业株式会社 | 金属材料及其制造方法 |
| CN108480156A (zh) * | 2018-06-01 | 2018-09-04 | 深圳市金中瑞通讯技术有限公司 | 一种喷涂方法及喷枪 |
| RU196347U1 (ru) * | 2019-03-18 | 2020-02-26 | Сергей Львович Балдаев | Стальная нефтепромысловая труба |
| CN111471950A (zh) * | 2020-03-31 | 2020-07-31 | 中煤科工集团西安研究院有限公司 | 双金属配油套超音速热喷涂制造方法 |
| CN112852254A (zh) * | 2020-12-30 | 2021-05-28 | 镇江市润发铝业有限公司 | 一种高强耐腐蚀型复合铝箔及其制备方法 |
| KR102729064B1 (ko) * | 2023-01-10 | 2024-11-13 | (주)코미코 | 대기 플라즈마 용사법에 의한 고밀도의 이트리아 피막의 제조 방법 및 이를 이용하여 제조된 이트리아 용사 피막 |
| US12326203B2 (en) | 2023-06-30 | 2025-06-10 | Halliburton Energy Services, Inc. | Downhole tool with crack compliant seal and mechanical strengthening feature at a joint thereof |
| US12326046B2 (en) | 2023-06-30 | 2025-06-10 | Halliburton Energy Services, Inc. | Downhole tool with crack compliant seal and high yield strength weld positioned at a joint thereof |
| CN118207480A (zh) * | 2024-04-17 | 2024-06-18 | 南通市嘉业机械制造有限公司 | 一种耐腐蚀无缝钢管穿孔顶头及其制备工艺 |
| CN119663160A (zh) * | 2024-12-05 | 2025-03-21 | 国网山东省电力公司电力科学研究院 | 一种架空输电线路连接金具制备方法及连接金具 |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH06330263A (ja) * | 1993-05-24 | 1994-11-29 | Sumitomo Light Metal Ind Ltd | 高靭性Al−Si系合金の製造方法 |
| JPH101766A (ja) | 1996-06-11 | 1998-01-06 | Nippon Steel Corp | 耐食性及び耐傷付き性に優れた溶射皮膜 |
| JP2001247953A (ja) | 2000-03-08 | 2001-09-14 | Tocalo Co Ltd | 耐食性に優れた溶射被覆部材およびその製造方法 |
| JP2002053943A (ja) * | 2000-08-07 | 2002-02-19 | Toshiba Corp | 耐食コーティング部材 |
| JP2007131952A (ja) * | 2004-03-25 | 2007-05-31 | Akihisa Inoue | 金属ガラス積層体 |
| JP2008043869A (ja) * | 2006-08-14 | 2008-02-28 | Nakayama Steel Works Ltd | 過冷却液相金属皮膜の形成用溶射装置 |
| JP2010022895A (ja) * | 2008-07-15 | 2010-02-04 | Nakayama Steel Works Ltd | アモルファス皮膜の形成装置および形成方法 |
| WO2013105613A1 (ja) * | 2012-01-13 | 2013-07-18 | 株式会社中山製鋼所 | アモルファス皮膜の形成装置および形成方法 |
Family Cites Families (36)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4593007A (en) * | 1984-12-06 | 1986-06-03 | The Perkin-Elmer Corporation | Aluminum and silica clad refractory oxide thermal spray powder |
| JP2826220B2 (ja) * | 1991-09-19 | 1998-11-18 | トーカロ株式会社 | 溶融亜鉛浴用部材 |
| US20030088980A1 (en) * | 1993-11-01 | 2003-05-15 | Arnold James E. | Method for correcting defects in a workpiece |
| EP0806488B1 (en) * | 1996-05-08 | 2002-10-16 | Denki Kagaku Kogyo Kabushiki Kaisha | Aluminum-chromium alloy, method for its production and its applications |
| ATE273401T1 (de) * | 1996-12-23 | 2004-08-15 | James E Arnold | Verfahren zur behandlung von metallteilen |
| US5820939A (en) * | 1997-03-31 | 1998-10-13 | Ford Global Technologies, Inc. | Method of thermally spraying metallic coatings using flux cored wire |
| DE19733204B4 (de) * | 1997-08-01 | 2005-06-09 | Daimlerchrysler Ag | Beschichtung aus einer übereutektischen Aluminium/Silizium Legierung, Spritzpulver zu deren Herstellung sowie deren Verwendung |
| US6231969B1 (en) * | 1997-08-11 | 2001-05-15 | Drexel University | Corrosion, oxidation and/or wear-resistant coatings |
| JP4648541B2 (ja) * | 1998-03-14 | 2011-03-09 | ダナ・コーポレイション | すべり軸受のライニングの形成方法 |
| USH1869H (en) * | 1998-12-18 | 2000-10-03 | Caterpillar Inc. | Valve train components having an oxidation and corrosion-resistant thermal spray coating |
| US6372299B1 (en) * | 1999-09-28 | 2002-04-16 | General Electric Company | Method for improving the oxidation-resistance of metal substrates coated with thermal barrier coatings |
| US20020073982A1 (en) * | 2000-12-16 | 2002-06-20 | Shaikh Furqan Zafar | Gas-dynamic cold spray lining for aluminum engine block cylinders |
| JP4036387B2 (ja) * | 2001-05-11 | 2008-01-23 | 日鐵溶接工業株式会社 | レーザアシスト高速フレーム溶射法および装置 |
| US20030049485A1 (en) * | 2001-09-06 | 2003-03-13 | Brupbacher John M. | Corrosion control coatings |
| EP2479309B1 (en) | 2004-03-25 | 2016-05-11 | Tohoku Techno Arch Co., Ltd. | Metallic glass laminates, production methods and applications thereof |
| FR2877015B1 (fr) * | 2004-10-21 | 2007-10-26 | Commissariat Energie Atomique | Revetement nanostructure et procede de revetement. |
| US20090194233A1 (en) * | 2005-06-23 | 2009-08-06 | Tokyo Electron Limited | Component for semicondutor processing apparatus and manufacturing method thereof |
| EP1762639A1 (en) * | 2005-09-13 | 2007-03-14 | Kabushiki Kaisha Kobe Seiko Sho (Kobe Steel, Ltd.) | Heat transfer tube for LNG vaporizer, its production method, and LNG vaporizer using such heat transfer tubes |
| DE102005047037A1 (de) * | 2005-09-30 | 2007-04-19 | BAM Bundesanstalt für Materialforschung und -prüfung | Motorische Gleitpaarung aus einer Aluminiumbasislegierung |
| EP2060652B1 (en) * | 2006-08-14 | 2013-11-27 | Nakayama Amorphous Co., Ltd. | Method and apparatus for forming amorphous coating film |
| JP5190238B2 (ja) * | 2006-09-28 | 2013-04-24 | 新日鐵住金株式会社 | 高耐食性防錆塗料、高耐食性鉄鋼材料及び鋼構造物 |
| US20110159138A1 (en) * | 2007-01-08 | 2011-06-30 | Garrtech Inc. | Blow mold for molding a container |
| US7904491B2 (en) * | 2007-07-18 | 2011-03-08 | Sap Ag | Data mapping and import system |
| DE102008026101B4 (de) * | 2008-05-30 | 2010-02-18 | Fraunhofer-Gesellschaft zur Förderung der angewandten Forschung e.V. | Thermisch gespritzte Al2O3-Schichten mit einem hohen Korundgehalt ohne eigenschaftsmindernde Zusätze und Verfahren zu ihrer Herstellung |
| US8313557B2 (en) * | 2008-07-30 | 2012-11-20 | The United States Of America, As Represented By The Secretary Of The Navy | Recovery of [CO2]T from seawater/aqueous bicarbonate systems using a multi-layer gas permeable membrane |
| US9611522B2 (en) * | 2009-05-06 | 2017-04-04 | United Technologies Corporation | Spray deposition of L12 aluminum alloys |
| US20110064963A1 (en) * | 2009-09-17 | 2011-03-17 | Justin Lee Cheney | Thermal spray processes and alloys for use in same |
| CN102791384B (zh) * | 2010-01-13 | 2015-11-25 | 株式会社中山非晶体 | 用于形成非晶体涂层膜的装置和方法 |
| US20130101820A1 (en) * | 2010-05-24 | 2013-04-25 | Nobuo Yonekura | Thermal spray coated member and thermal spraying method therefor |
| US9194039B2 (en) * | 2011-03-15 | 2015-11-24 | Directed Vapor Technologies International | Method for applying aluminum alloy coatings for corrosion protection of steel |
| JP5973790B2 (ja) * | 2012-05-28 | 2016-08-23 | 株式会社中山アモルファス | 耐食性、導電性、成形性に優れた薄板およびその製造方法 |
| KR101519709B1 (ko) * | 2013-03-05 | 2015-05-12 | 기아자동차주식회사 | 고속화염용사 코팅법과 플라즈마 이온 질화법를 이용한 금형의 보정 및 재생 방법 |
| WO2015053948A1 (en) * | 2013-10-09 | 2015-04-16 | United Technologies Corporation | Aluminum alloy coating with rare earth and transition metal corrosion inhibitors |
| US10392685B2 (en) * | 2013-10-31 | 2019-08-27 | The Regents Of The University Of Michigan | Composite metal alloy material |
| JP6367567B2 (ja) * | 2014-01-31 | 2018-08-01 | 吉川工業株式会社 | 耐食性溶射皮膜、その形成方法およびその形成用溶射装置 |
| CN107083502B (zh) * | 2016-02-12 | 2023-10-13 | 肯纳金属公司 | 耐磨且耐蚀的钴基合金粉末及其施加方法 |
-
2014
- 2014-01-31 JP JP2014017943A patent/JP6367567B2/ja active Active
-
2015
- 2015-01-27 EP EP15742600.8A patent/EP3101151B1/en active Active
- 2015-01-27 WO PCT/JP2015/052111 patent/WO2015115394A1/ja not_active Ceased
- 2015-01-27 ES ES15742600T patent/ES2797741T3/es active Active
- 2015-01-27 US US15/115,746 patent/US10323153B2/en active Active
- 2015-01-27 CN CN201580006682.XA patent/CN106062236A/zh active Pending
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH06330263A (ja) * | 1993-05-24 | 1994-11-29 | Sumitomo Light Metal Ind Ltd | 高靭性Al−Si系合金の製造方法 |
| JPH101766A (ja) | 1996-06-11 | 1998-01-06 | Nippon Steel Corp | 耐食性及び耐傷付き性に優れた溶射皮膜 |
| JP2001247953A (ja) | 2000-03-08 | 2001-09-14 | Tocalo Co Ltd | 耐食性に優れた溶射被覆部材およびその製造方法 |
| JP2002053943A (ja) * | 2000-08-07 | 2002-02-19 | Toshiba Corp | 耐食コーティング部材 |
| JP2007131952A (ja) * | 2004-03-25 | 2007-05-31 | Akihisa Inoue | 金属ガラス積層体 |
| JP2008043869A (ja) * | 2006-08-14 | 2008-02-28 | Nakayama Steel Works Ltd | 過冷却液相金属皮膜の形成用溶射装置 |
| JP2010022895A (ja) * | 2008-07-15 | 2010-02-04 | Nakayama Steel Works Ltd | アモルファス皮膜の形成装置および形成方法 |
| WO2013105613A1 (ja) * | 2012-01-13 | 2013-07-18 | 株式会社中山製鋼所 | アモルファス皮膜の形成装置および形成方法 |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2017122253A (ja) * | 2016-01-05 | 2017-07-13 | 吉川工業株式会社 | 金属溶射皮膜及びその作製方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| US20170015838A1 (en) | 2017-01-19 |
| US10323153B2 (en) | 2019-06-18 |
| JP6367567B2 (ja) | 2018-08-01 |
| CN106062236A (zh) | 2016-10-26 |
| EP3101151A4 (en) | 2017-11-01 |
| EP3101151B1 (en) | 2020-06-03 |
| ES2797741T3 (es) | 2020-12-03 |
| EP3101151A1 (en) | 2016-12-07 |
| JP2015145516A (ja) | 2015-08-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6367567B2 (ja) | 耐食性溶射皮膜、その形成方法およびその形成用溶射装置 | |
| Tang et al. | Effects of surface oxidation during HVOF processing on the primary stage oxidation of a CoNiCrAlY coating | |
| CN102906298B (zh) | 热喷涂件以及热喷涂件的热喷涂方法 | |
| CN103801893B (zh) | 一种用于船舶螺旋桨腐蚀修复与长效防护的方法 | |
| US20130216722A1 (en) | Coating Compositions, Applications Thereof, and Methods of Forming | |
| JP2018506644A (ja) | 溶接性及び加工部耐食性に優れた亜鉛合金めっき鋼材及びその製造方法 | |
| JP3612568B2 (ja) | Hvof溶射ガンによる金属皮膜形成方法と溶射装置 | |
| CN109440052A (zh) | 一种大气等离子体喷涂氧化钇涂层的复合涂层制备方法 | |
| CN101353797B (zh) | 大功率电弧喷涂锌铝伪合金防护膜的喷涂方法 | |
| Park et al. | Electrochemical characteristics in seawater for cold thermal spray-coated Al–Mg alloy layer | |
| JP6500136B2 (ja) | 耐食性溶射皮膜、その形成方法およびその形成用溶射装置 | |
| CN106567027A (zh) | 一种金属管道镍基复合耐蚀涂层及其制备方法 | |
| JP2008174784A (ja) | 溶射によるアモルファス皮膜の形成方法 | |
| JP6594209B2 (ja) | 金属溶射皮膜の作製方法 | |
| RU2489512C2 (ru) | Способ антикоррозионной обработки детали путем осаждения слоя циркония и/или циркониевого сплава | |
| CN108842128A (zh) | 一种含陶瓷颗粒铝基复合粉芯丝材及涂层的制备方法 | |
| JP5098109B2 (ja) | 皮膜形成方法 | |
| JP2014237864A (ja) | 被覆部材の製造方法及び被覆部材 | |
| Kawakita et al. | Corrosion resistance of HastelloyC coatings formed by an improved HVOF thermal spraying process | |
| TW201418376A (zh) | 防止海洋生物污損的複合塗層及其噴塗方法 | |
| US20130216862A1 (en) | Coating Compositions, Applications Thereof, and Methods of Forming | |
| JP4172653B2 (ja) | 耐海水防食方法 | |
| Kawakita et al. | Oscillational corrosion potential of HastelloyC coatings fabricated by GS-HVOF spraying | |
| JP4751206B2 (ja) | 高耐食性めっき鋼材及びその製造方法 | |
| Dong et al. | Long-Term Corrosion Behavior of Atmospheric Plasma Sprayed NiCr Alloy Containing Boron in 3.5 wt.% NaCl Solution |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| DPE1 | Request for preliminary examination filed after expiration of 19th month from priority date (pct application filed from 20040101) | ||
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 15115746 Country of ref document: US |
|
| REEP | Request for entry into the european phase |
Ref document number: 2015742600 Country of ref document: EP |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2015742600 Country of ref document: EP |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 15742600 Country of ref document: EP Kind code of ref document: A1 |