WO2016047508A1 - 積層型硬質皮膜および成形用金型 - Google Patents
積層型硬質皮膜および成形用金型 Download PDFInfo
- Publication number
- WO2016047508A1 WO2016047508A1 PCT/JP2015/076204 JP2015076204W WO2016047508A1 WO 2016047508 A1 WO2016047508 A1 WO 2016047508A1 JP 2015076204 W JP2015076204 W JP 2015076204W WO 2016047508 A1 WO2016047508 A1 WO 2016047508A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- layer
- hard coating
- film
- atomic ratio
- wear resistance
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D37/00—Tools as parts of machines covered by this subclass
- B21D37/01—Selection of materials
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D37/00—Tools as parts of machines covered by this subclass
- B21D37/20—Making tools by operations not covered by a single other subclass
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C14/00—Coating by vacuum evaporation, by sputtering or by ion implantation of the coating forming material
- C23C14/06—Coating by vacuum evaporation, by sputtering or by ion implantation of the coating forming material characterised by the coating material
Definitions
- the present invention relates to a laminated hard coating exhibiting excellent wear resistance and toughness, and a molding die having the laminated hard coating on the substrate surface.
- hard coatings such as TiN, TiCN and TiAlN have been applied to the surface of the base material for the purpose of improving the wear resistance of jigs and tools made of cemented carbide, cermet, high speed tool steel or alloy tool steel.
- the coating is done on.
- realization of a hard coating with further improved wear resistance is demanded as the work material is hardened and the cutting speed is increased.
- the present inventor has proposed a hard film in which a film layer satisfying a predetermined composition ratio is laminated on the surface of a mold base for forming a steel material typified by high-tensile steel as shown in Patent Document 1, for example. ing.
- the present invention has been made in view of the circumstances as described above, and an object of the present invention is to provide a laminated hard film and a molding die with further improved wear resistance and toughness.
- the atomic ratio of Al in the total amount of Ti, Cr, Al and Si in the layer A and the layer B is preferably in the range of 0.20 to 0.60.
- the laminated hard coating of the present invention it is also useful to substitute at least a part of Ti in the layer A with Zr.
- a molding die with further improved wear resistance and toughness can be realized.
- a molding die having a CrN intermediate layer with a thickness of 3 to 10 ⁇ m between the laminated hard coating and the substrate is also preferable.
- such a molding die is particularly useful as a die used for hot forming of steel materials because it exhibits characteristics that are leaked not only at room temperature but also at a high temperature of about 400 to 500 ° C.
- the layered hard film obtained by laminating the layer A exhibiting good wear resistance and the layer B exhibiting high toughness is more wear resistant and tougher than the conventional single layer type hard film. Can be further improved.
- the hard coating of the present invention is characterized in that it is a laminated hard coating in which layers A exhibiting good wear resistance and layers B exhibiting high toughness are alternately stacked.
- the layer A contains a predetermined amount of Al, so that it exhibits excellent wear resistance when forming a steel material in which a scale is generated on the surface in a hot forming region where the sliding property with the steel material is high, particularly in a high temperature.
- the atomic ratio of Al 0.50 or more i.e., (Ti a Cr b Al c Si d) (C x N 1-x) Ti in the layer A indicated by, Cr, Al and
- the value of c needs to be 0.50 or more.
- the value of c is preferably 0.60 or more, more preferably 0.65 or more.
- the value of c needs to be 0.90 or less.
- the value of c is preferably 0.85 or less, more preferably 0.80 or less.
- Ti in the layer A may not be contained in the film, but by including Ti, the hardness of the film is increased and the wear resistance is further improved.
- the atomic ratio of Ti that is, the value of a is preferably 0.01 or more, and more preferably 0.02 or more.
- the atomic ratio of Ti that is, the value of a needs to be 0.10 or less.
- the value of a is preferably 0.08 or less, more preferably 0.05 or less.
- the Cr in the layer A increases the hardness of the film and improves the wear resistance. From such a viewpoint, the atomic ratio of Cr, that is, the value of b needs to be 0.10 or more.
- the value of b is preferably 0.15 or more, more preferably 0.20 or more.
- the atomic ratio of Cr, that is, the value of b needs to be 0.50 or less.
- the value of b is preferably 0.45 or less, more preferably 0.40 or less.
- the metal element other than Ti, Cr and Al in the layer A is Si.
- Si is an element effective in increasing the hardness of the film and improving the wear resistance, and is contained if necessary.
- the Si atomic ratio, that is, the value of d is preferably 0.01 or more, and more preferably 0.02 or more.
- the Si atomic ratio, that is, the value of d needs to be 0.05 or less.
- the value of d is preferably 0.04 or less, more preferably 0.03 or less.
- carbon C may be contained as an impurity in the film, and in this case, a part of carbide is formed.
- the atomic ratio of C that is, the value of x needs to be 0.5 or less.
- the value of x is preferably 0.3 or less, more preferably 0.1 or less.
- the layer B constituting the laminated hard coating of the present invention is (Cr e Si 1-e ) (C y N 1-y ), and when the atomic ratio of Cr and C is e and y, respectively, 0.90 ⁇ e ⁇ 1.0, 0 ⁇ y ⁇ 0.5
- it is composed of (Al f Si 1-f ) (C z N 1-z ), and the following relationship is satisfied when the atomic ratio of Al and C is f and z, respectively. 0.90 ⁇ f ⁇ 1.0, 0 ⁇ z ⁇ 0.5
- the layer B contains Cr or Al as a metal element, it exhibits high toughness. Specifically, it exhibits the characteristic that the chipping of the film hardly occurs under a high load.
- the atomic ratio of Cr or Al that is, the value of e or f needs to be 0.90 or more.
- the value of e or f is preferably 0.93 or more, more preferably 0.95 or more.
- the layer B may be composed only of Cr or Al, but a part of Cr or Al may be replaced with Si.
- Si is an element effective in increasing the hardness of the film and improving the wear resistance, and is contained if necessary. However, if the amount of Si is excessive, the Cr or Al content is relatively insufficient, and the toughness of the layer B is lowered, and the hardness is lowered and the wear resistance is lowered. That is, the value of 1-e or 1-f must be 0.10 or less. The value of 1-e or 1-f is preferably 0.07 or less, more preferably 0.05 or less.
- a hard film having both excellent wear resistance and toughness can be realized by alternately laminating layer A having excellent wear resistance and layer B having excellent toughness.
- layer A and B In order to effectively exhibit the functions of the layers A and B, it is necessary to alternately stack the layers A and B as independent layers, instead of mixing the compositions of the layers A and B. .
- the thicknesses of the layer A and the layer B must each be 2 nm or more.
- the thicknesses of the layer A and the layer B are each preferably 5 nm or more, more preferably 10 nm or more.
- the thicknesses of the layer A and the layer B need to be 100 nm or less, respectively.
- the thickness of each of layer A and layer B is preferably 50 nm or less, more preferably 40 nm or less, still more preferably 30 nm or less, and particularly preferably 20 nm or less.
- the thicknesses of the layer A and the layer B are not necessarily the same.
- the thickness of the layer A can be 20 nm
- the thickness of the layer B can be changed to 2 to 100 nm.
- the base material side does not necessarily need to be the layer B, and the layer A may exist in the base material side.
- the layer A or the layer B present on the substrate side may be a film structure present on the outermost surface side, and various laminated structures can be formed according to the purpose.
- layer A / B1 (CrSiCN) / layer A / layer B (AlSiCN) / layer A. ⁇ ” can also be used.
- the thickness of the entire laminated hard coating is not limited at all.
- the total thickness of the coating is preferably 1 ⁇ m (1000 nm) or more, more preferably 2 ⁇ m (2000 nm) or more.
- the toughness of the film deteriorates when the total thickness of the film becomes too thick, it is preferably 20 ⁇ m (20000 nm) or less, more preferably 10 ⁇ m (10000 nm) or less, and even more preferably 8 ⁇ m (8000 nm) or less. is there.
- it is recommended that the number of times the layer A and the layer B are stacked is appropriately controlled so as to satisfy the preferable overall thickness described above.
- the number of stacking is a plurality of two or more. From such a viewpoint, it is preferable that the thickness of each of the layer A and the layer B is made as thin as possible so that the number of laminations is plural.
- the number of laminations is a value when the number of laminations of layer A and layer B is 1.
- the ratio of elements in each layer of layer A and layer B is as described above.
- the total amount of metal elements in layers A and B that is, Ti, Cr
- the atomic ratio of Al in the total amount of Al and Si greatly affects the wear resistance.
- the “atomic ratio of Al in the total amount of Ti, Cr, Al, and Si in layers A and B” may be referred to as “total Al atomic ratio”.
- the total Al atomic ratio is preferably in the range of 0.20 to 0.60 in order to ensure better wear resistance.
- the lower limit of the total Al atomic ratio is more preferably 0.30 or more, still more preferably 0.35 or more, and still more preferably 0.40 or more.
- the upper limit of the total Al atomic ratio is more preferably 0.55 or less.
- the total Al atomic ratio can be calculated as follows.
- the laminated hard coating of the present invention will be described by taking the combination of the following layer A1 and layer B1 as an example.
- the layer A1 and the layer B1 have the same crystal structure.
- the atomic ratio of Al in the total amount of Cr and Al in the layers A1 and B1 (1 / ⁇ ) 3 ⁇ 4 ⁇ c ⁇ q / [(1 / ⁇ ) 3 ⁇ 4 ⁇ c ⁇ q + (1 / ⁇ ) 3 ⁇ 4 ⁇ (1-c) ⁇ q + (1 / ⁇ ) 3 ⁇ 4 ⁇ r]
- the total Al atomic ratio is calculated as described above. Can be sought. When the crystal structure is unknown, the calculation as described above cannot be performed. Therefore, the formed layer A and layer B may be measured by EDX, and the total Al atomic ratio may be obtained using the measurement result.
- the layer A it is also effective to substitute at least a part of Ti in the layer A with Zr. This further improves the wear resistance of layer A. Such an effect increases as the amount of Zr to be replaced increases. This is because the film component is oxidized by the heat generated during sliding when used as a molding die, and a hard oxide film containing Zr on the surface is generated.
- the ratio of substituting Ti with Zr is not particularly limited, but is preferably at least 10% or more with respect to the Ti amount. All of the Ti amount may be replaced with Zr.
- the preferable range of the atomic ratio of Zr is the same as the range of a in the case of containing only Ti without containing Zr. That is, when Zr is contained instead of Ti, the atomic ratio of Zr is preferably 0.01 or more, more preferably 0.02 or more with respect to the entire metal element of the layer A.
- the atomic ratio of Zr is preferably 0.10 or less. More preferably, it is 0.08 or less, More preferably, it is 0.05 or less.
- the molding die of the present invention exhibits excellent characteristics even at high temperatures, and is particularly useful as a die used for hot forming of steel materials.
- the molding die of the present invention may have CrN with a thickness of 3 to 10 ⁇ m as an intermediate layer between the laminated hard coating and the base material, that is, immediately above the base material. Thereby, excellent wear resistance and toughness are exhibited while ensuring good adhesion between the laminated hard coating and the substrate surface.
- the thickness of the intermediate layer is preferably 3 ⁇ m or more from the viewpoint of ensuring adhesion.
- the thickness be 10 ⁇ m or less. More preferably, it is 5 ⁇ m or more and 8 ⁇ m or less.
- the type of the base material used for the molding die is not particularly limited.
- WC—Co alloy, WC—TiC—Co alloy, WC—TiC— (TaC or NbC) —Co alloy, WC— (TaC or NbC) -Co-based alloys such as tungsten carbide based cemented carbides; for example, cermet alloys such as TiC-Ni-Mo-based alloys and TiC-TiN-Ni-Mo-based alloys; for example, JIS G 4403 (2006) High-speed tool steel materials such as SKH51 and SKD61; for example, alloy tool steel materials such as SKS11 and SKD1 defined in JIS G 4404 (2006), and the like.
- the hard coating can be formed on the surface of the base material using a known method such as a physical vapor deposition method (PVD method: Physical vapor deposition process) or a chemical vapor deposition method (CVD method: Chemical vapor deposition process).
- PVD method Physical vapor deposition process
- CVD method Chemical vapor deposition process
- the PVD method is preferably used from the viewpoint of adhesion of the hard coating.
- an ion plating method such as an arc ion plating (AIP) method or a reactive PVD method such as a sputtering method is effective.
- AIP arc ion plating
- a reactive PVD method such as a sputtering method
- UBMS unbalanced magnetron sputtering
- the component composition of the target to be used determines the component composition of the film to be formed, and therefore the target component composition may be the same as the target film composition. preferable.
- Preferred conditions for film formation by the arc ion plating method include the following conditions, for example.
- the base-material temperature at the time of film-forming is 500 degrees C or less.
- Substrate temperature during film formation 300 ° C. or higher and 800 ° C. or lower
- the laminated hard coating of the present invention is suitable for use in molding dies due to its excellent wear resistance and toughness, but it can also be used as a hard coating formed on the surface of a cutting tool, for example, by taking advantage of its properties. Can be used.
- Example 1 A single-layer or multi-layer film having the composition shown in Table 1 below was formed using an AIP apparatus. At this time, the target corresponding to each metal part of the layer A and the layer B was used. Further, as the base material, a fine WC-Co type cemented carbide ball having a diameter of 10 mm having the same components as the fine grained cemented carbide HTi10 manufactured by Mitsubishi Materials Corporation was used with a mirror finish on the surface. In addition, the test No. in Table 1 below. For 1 to 31, a CrN film having a thickness of 5 ⁇ m was formed as an intermediate layer prior to the formation of the film. In addition, Test No. For No. 32, a film was formed directly on the substrate surface without forming an intermediate layer.
- the temperature of the base material as the object to be processed was heated to 400 ° C. with a heater installed in the chamber of the AIP apparatus, and the surface of the base material was cleaned with Ar ions.
- the cleaning conditions were as follows: atmosphere: Ar, pressure: 0.6 Pa, voltage: 500 V, time: 5 minutes.
- a nitrogen + methane atmosphere the pressure in the chamber is set to 4 Pa, arc discharge is started at a discharge current of 150 A, and a film having a total thickness of about 5 ⁇ m (about 5000 nm) is formed. Formed on a substrate.
- a bias voltage of 50 V was applied to the base material so that the substrate had a negative potential with respect to the ground potential.
- test no In the case of forming a laminated hard coating as shown in 5 to 32, targets having the composition of layer A and layer B are attached to separate evaporation sources, and the table on which the substrate is mounted is rotated in an AIP apparatus. Only the target of is discharged in a nitrogen atmosphere or in a nitrogen + methane atmosphere for a short time, and after forming the layer A on the surface of the intermediate layer or the substrate surface, the target of the layer B is discharged, and then the layer A and A multilayer film was formed by rotating the table while simultaneously discharging layer B.
- the layer A was formed on the surface of the intermediate layer or the surface of the base material, and then the layer B was formed.
- the performance is almost the same regardless of whether the layer A or the layer B exists on the base material side. .
- the thickness of layer A, the thickness of layer B, and the number of laminations in the multilayer film were adjusted by changing the rotation speed of the table. That is, if the rotation speed is increased, the thickness of the layer A and the thickness of the layer B are reduced, and the number of laminations is increased, and if the rotation speed is decreased, the thickness of the layer A and the thickness of the layer B is increased. Get smaller.
- test No. 1 in Table 1 was used.
- various types of single-layer coatings were also formed according to ordinary procedures.
- a sliding test was performed on the obtained balls of various coating coated cemented carbides under the following conditions to evaluate the wear resistance of the coating.
- an alumina plate was used as a substitute for the steel plate with scale as the following plate.
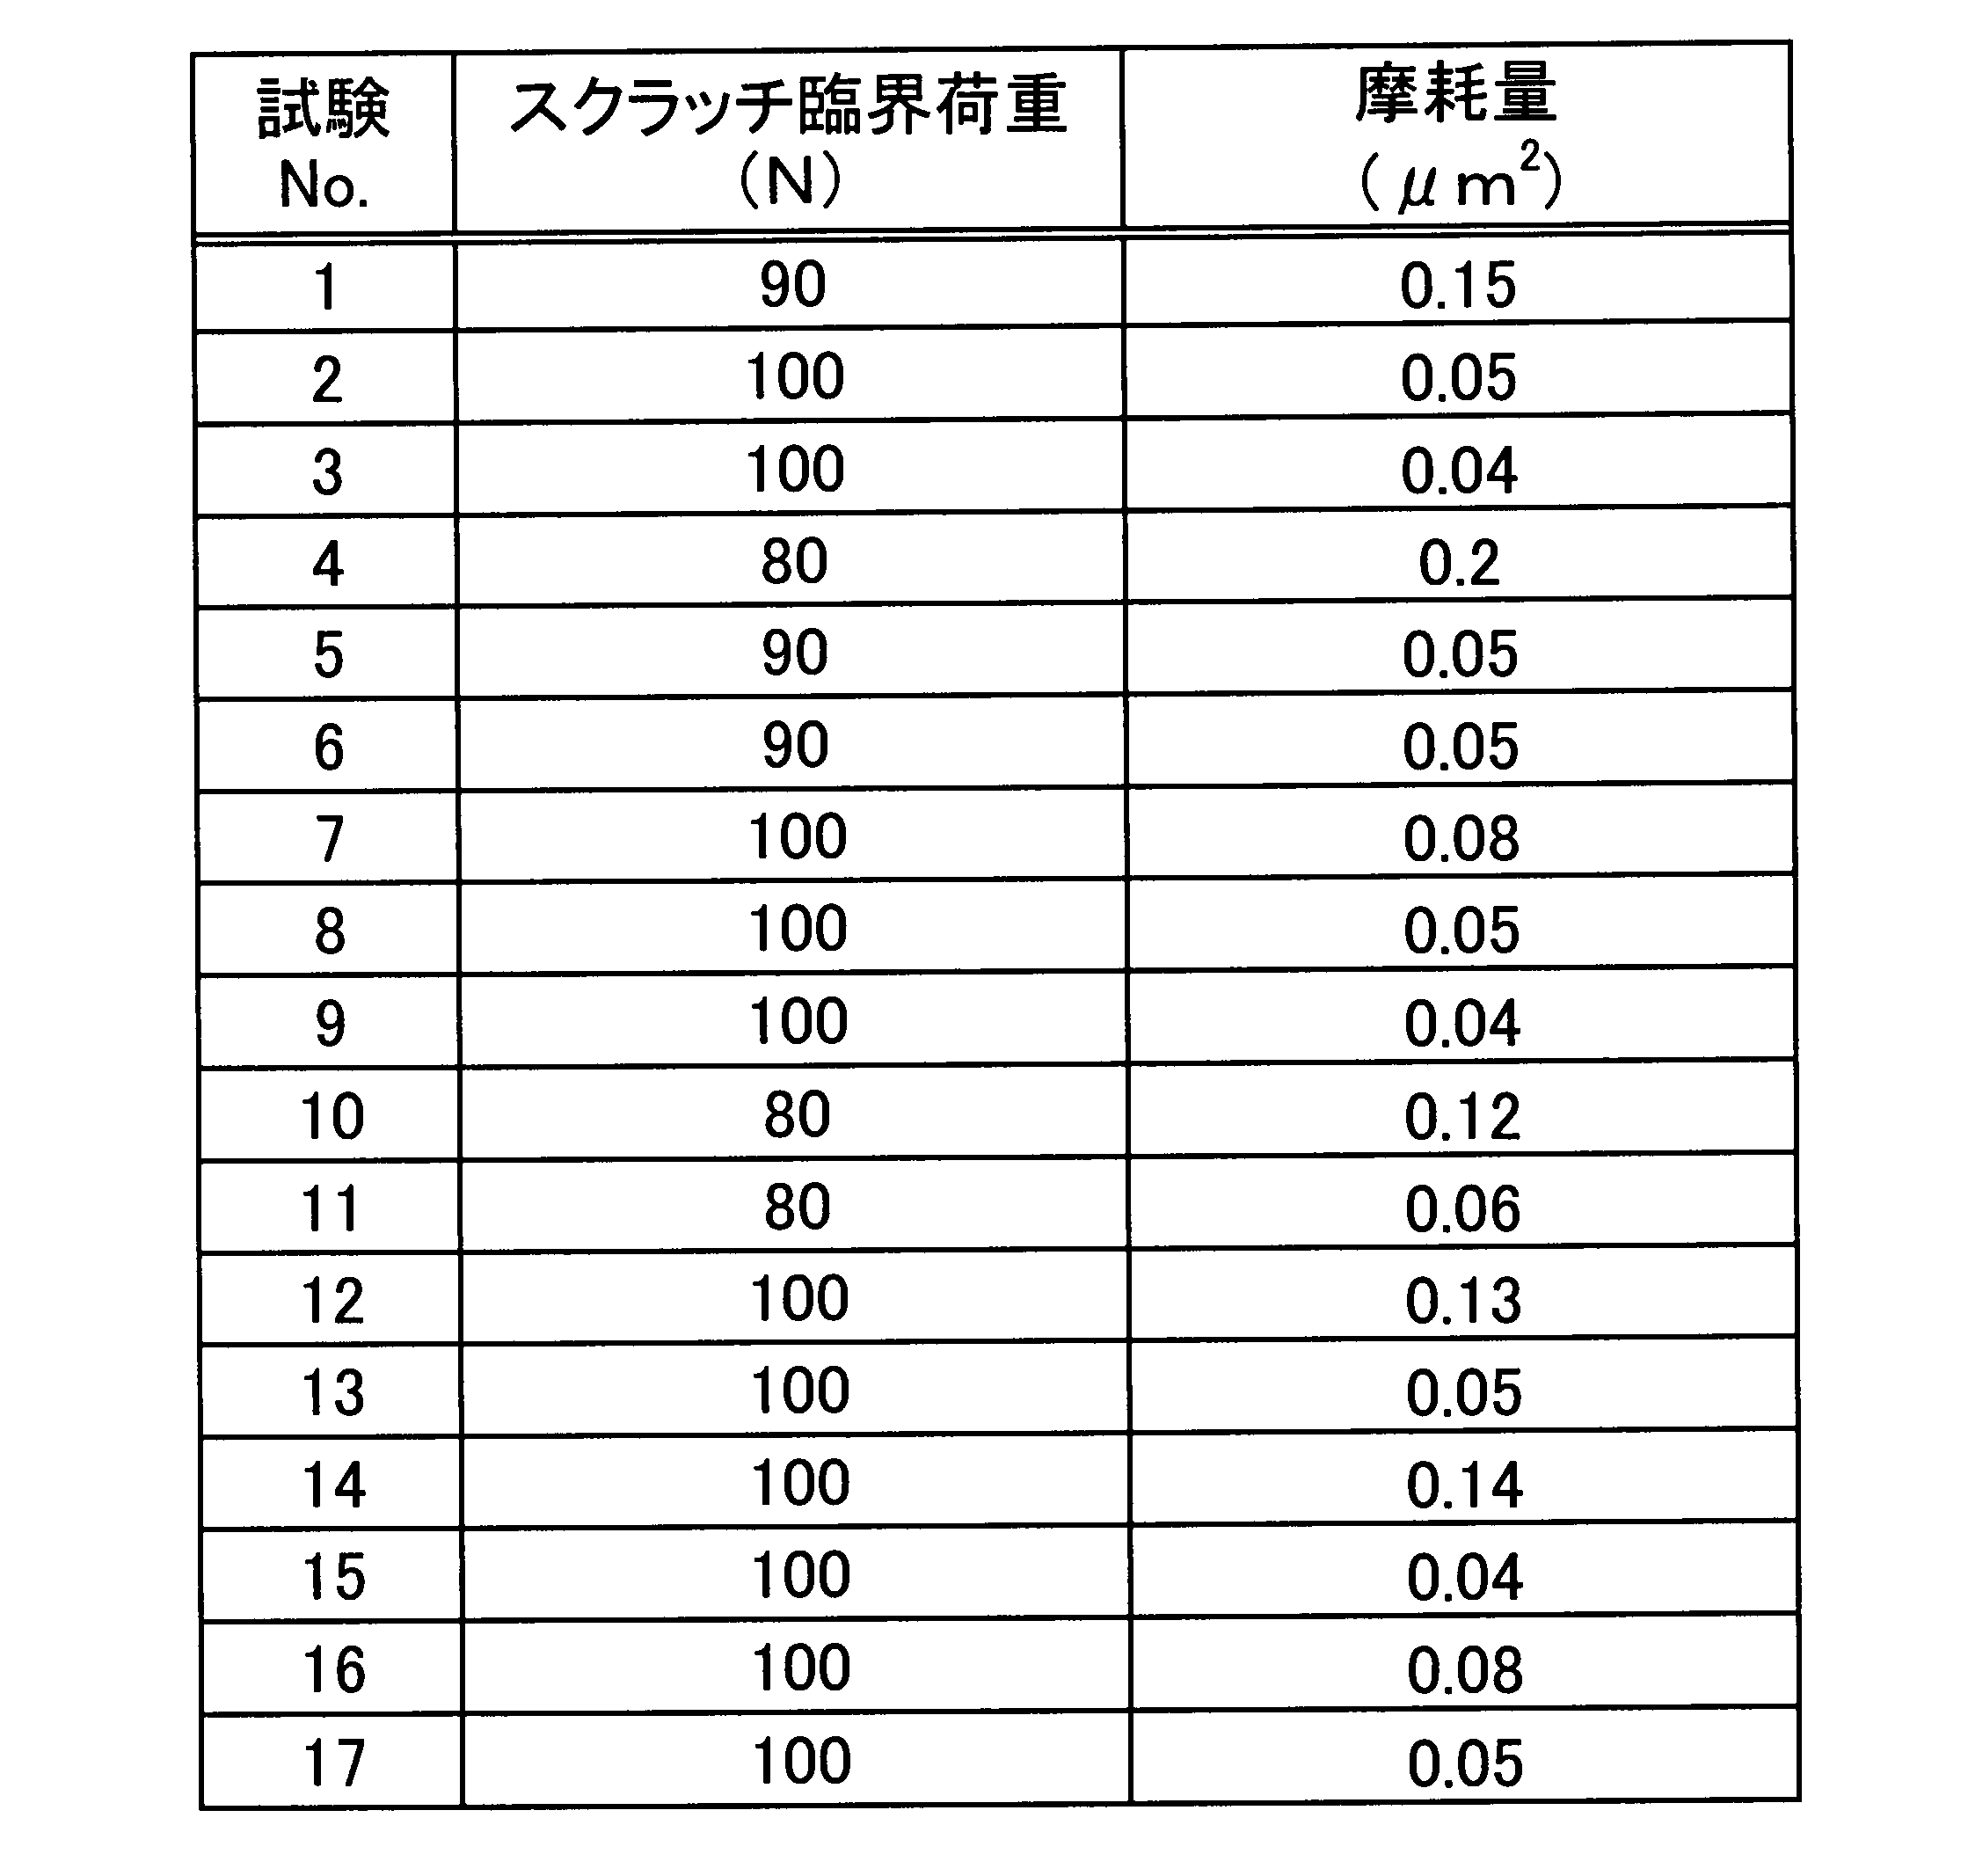
- the diameter of the wear part of the ball was measured, and the area corresponding to the diameter was evaluated as the wear amount. When the amount of wear was 0.4 ⁇ m 2 or less, it was evaluated that the wear resistance was excellent.
- each hard coating member was subjected to a scratch test under the following conditions to evaluate the toughness of the coating.
- the critical load at which chipping occurs in the film was measured. It was evaluated that the toughness was excellent when the critical load measurement value was 70 N or more.
- Test No. 6-11, 14-16, 18, 20, 22-25, 27-30, and 32 satisfy the ranges specified in the present invention for the composition of layer A and layer B, so that they have good wear resistance and It can be seen that it exhibits toughness.
- test no. 1 to 5, 12, 13, 17, 19, 21, 26, 31 do not satisfy any of the requirements defined in the present invention, and at least one of wear resistance and toughness is deteriorated. That is, test no.
- Reference numeral 1 denotes a conventional TiN monolayer film, which is deteriorated in both wear resistance and toughness.
- Test No. 2 is a conventional CrN single layer film, which has deteriorated wear resistance.
- Test No. Nos. 3 and 4 are examples in which a single layer type film composed only of the layer A is formed, and both wear resistance and toughness are deteriorated.
- Test No. No. 5 is an example in which the thickness of the layer A and the layer B is thin, and the wear resistance is deteriorated.
- Test No. No. 12 is an example in which the thickness of the layer A and the layer B is thick, and the wear resistance is deteriorated.
- Test No. 13 is an example in which the Al amount in the layer A is insufficient, and the wear resistance is deteriorated.
- Test No. 17 is an example in which the Al amount in the layer A is excessive, and the toughness is deteriorated.
- Test No. No. 19 is an example in which the Al amount in the layer A is insufficient and the Si amount is excessive, and the wear resistance is deteriorated.
- Test No. No. 21 is an example in which the Ti amount in the layer A is excessive and the Al amount is insufficient, and the wear resistance is deteriorated.
- Test No. No. 26 is an example in which the Cr amount in the layer B is small and the Si amount is excessive, and the wear resistance is deteriorated.
- Test No. No. 31 is an example in which the Al amount in the layer B is small and the Si amount is excessive, and the wear resistance is deteriorated.
- the sliding test and the scratch test were conducted at room temperature to evaluate the wear resistance and toughness of the film.
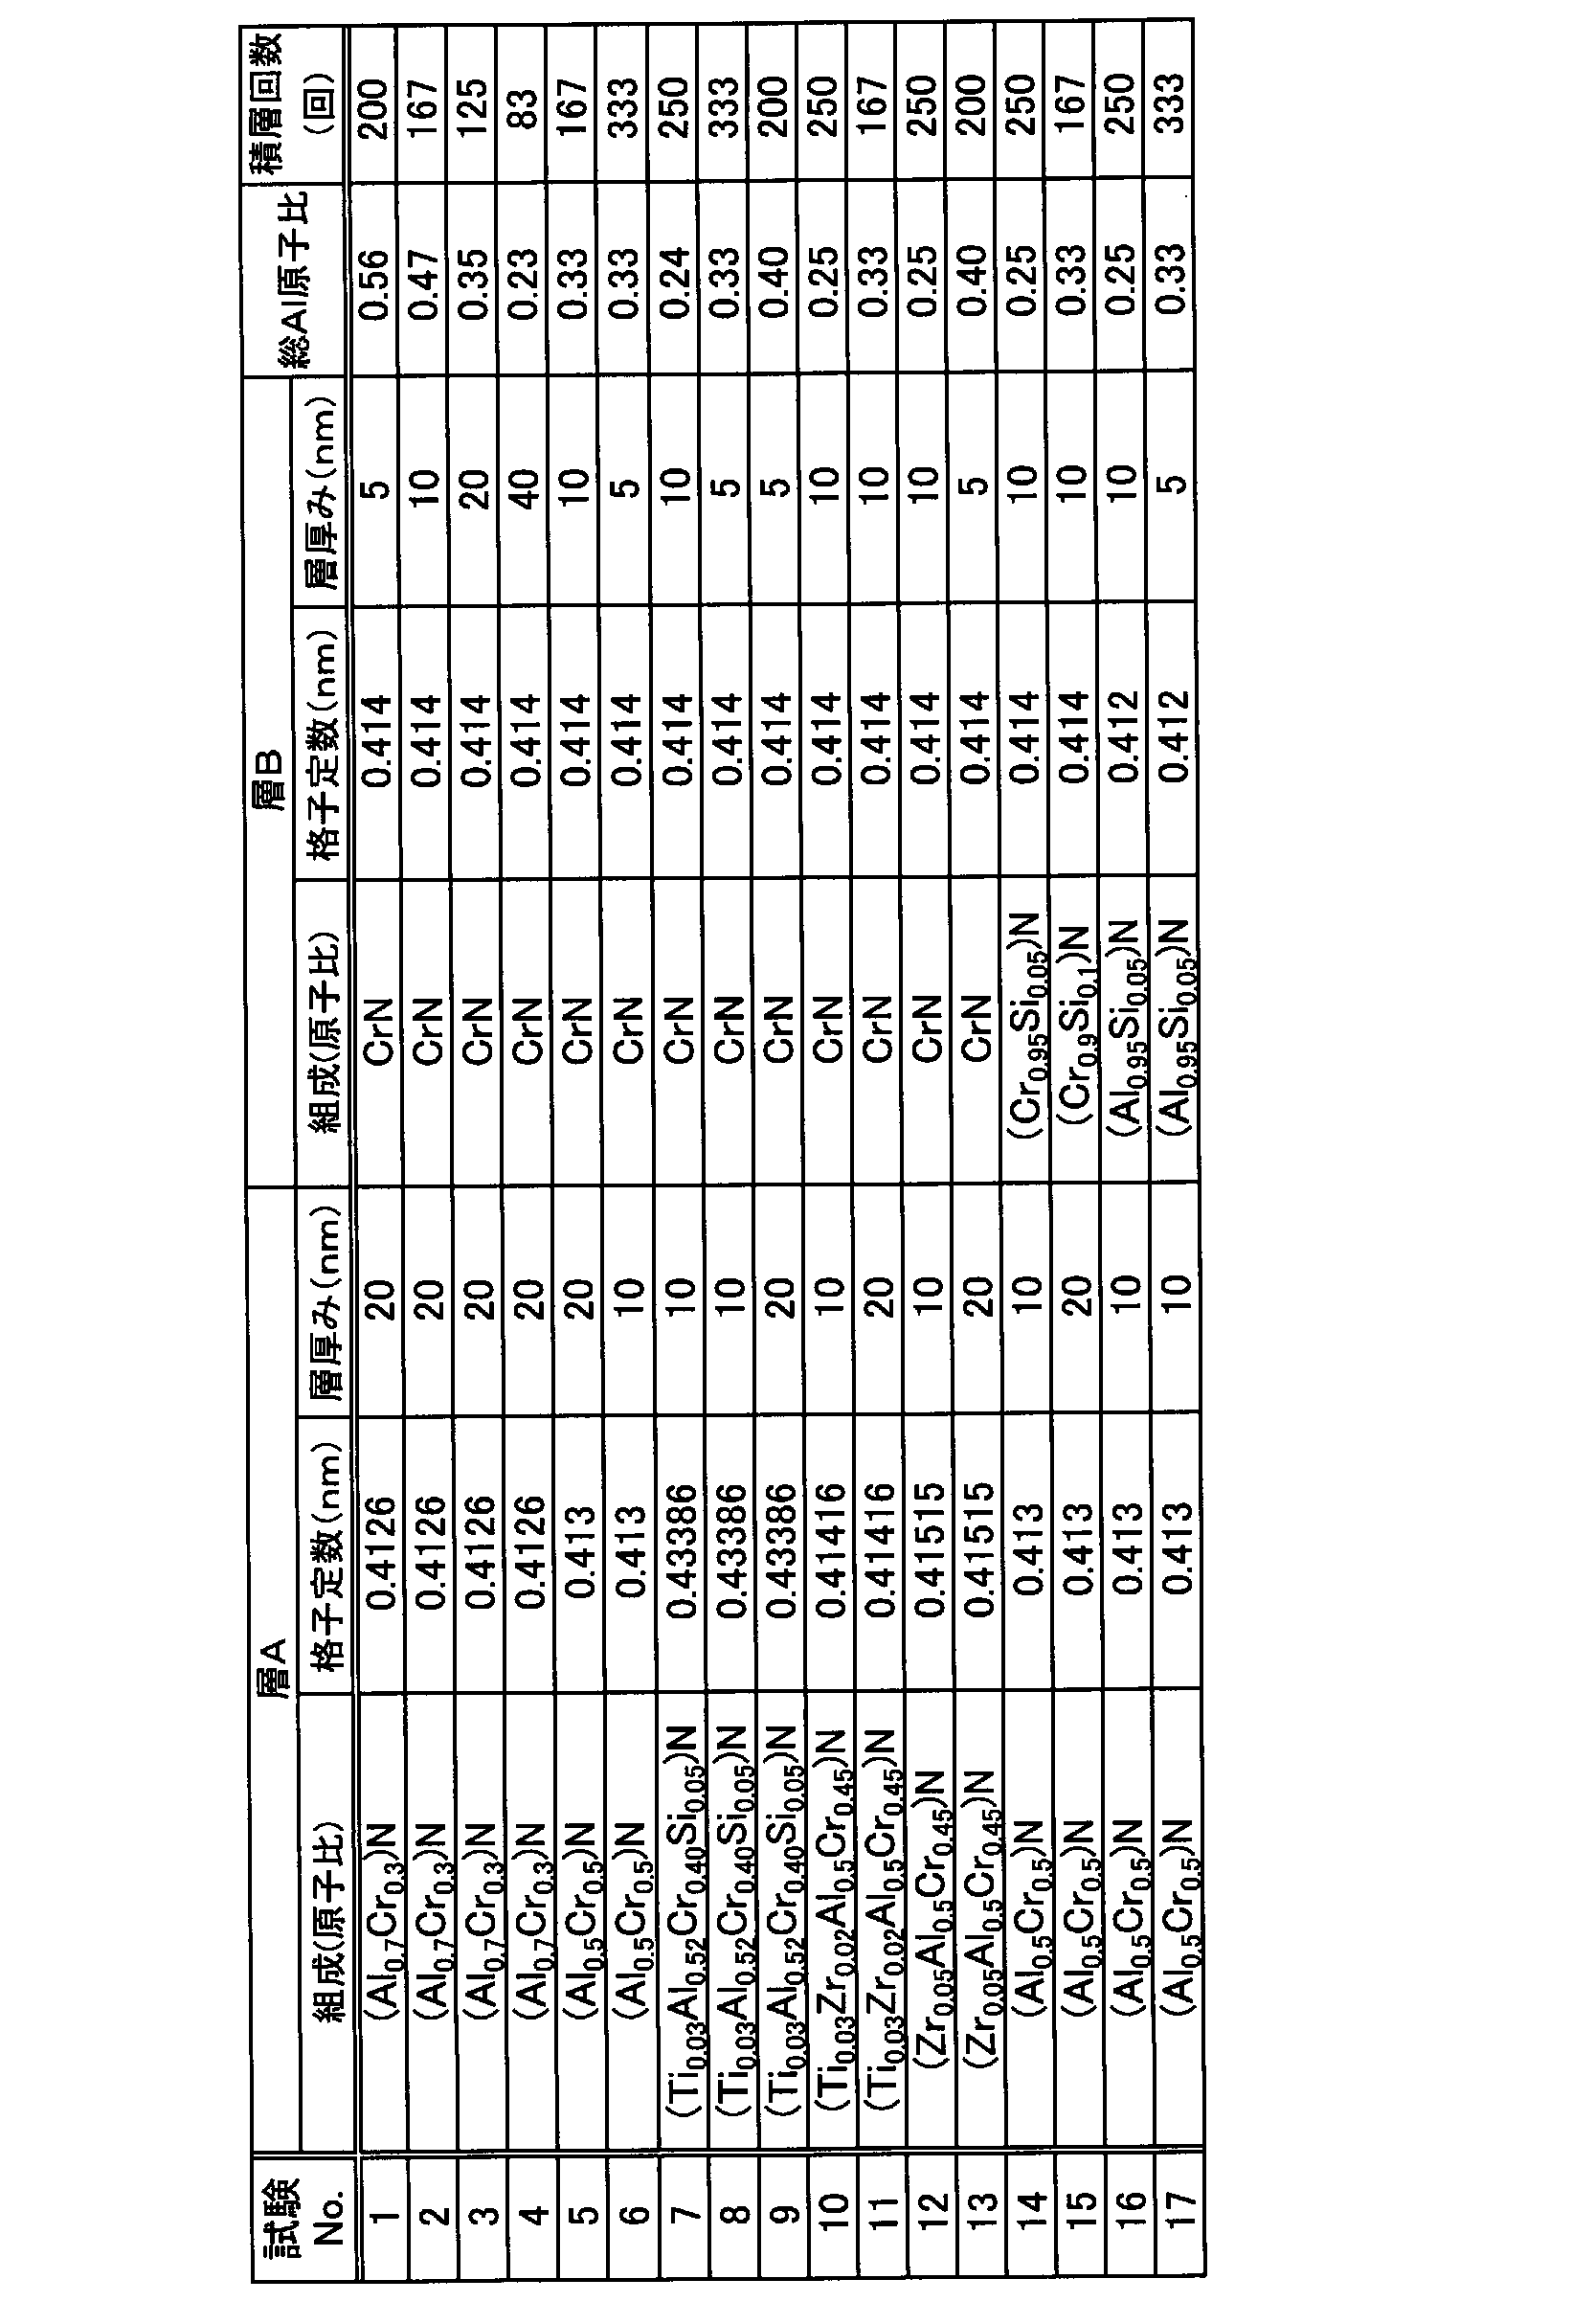
- Example 2 A laminated film having the composition shown in Table 3 below was formed in the same manner as in Example 1. In all the examples in Table 3 below, a CrN film having a thickness of 5 ⁇ m was formed as an intermediate layer prior to forming the film.
- Table 3 No. The film of No. 7 is No. 1 in Table 1. 22 is the same.
- No. No. 10 film is No. 1 in Table 1. 27, No. 3 in Table 3.
- No. 12 film is No. 1 in Table 1. 28, No. 3 in Table 3.
- No. 14 film is No. 1 in Table 1.
- 25 No. 3 in Table 3.
- No. 16 film is No. 1 in Table 1. 30 and the same.
- the total Al atomic ratio of the various coatings obtained was determined by the method described above from the composition of each layer, the lattice constant shown in Table 3, and the thickness of each layer. This total Al atomic ratio is shown in Table 3.
- a sliding test was conducted in the same manner as in Example 1 to evaluate the wear resistance of the various coated coating cemented carbide balls.
- a scratch test was performed on each hard coating member in the same manner as in Example 1 to evaluate the toughness of the coating.
- the laminated hard coating of the present invention has higher wear resistance and toughness, and is useful as a jig or tool for molding based on cemented carbide, cermet, high-speed tool steel or alloy tool steel. It is.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physical Vapour Deposition (AREA)
Abstract
Description
組成の異なる層Aと層Bが積層されてなる積層型硬質皮膜であって、
(TiaCrbAlcSid)(CxN1-x)からなり、
Ti、Cr、Al、SiおよびCの原子比を、夫々a、b、c、dおよびxとしたとき、0≦a≦0.10、0.10≦b≦0.50、0.50≦c≦0.90、0≦d≦0.05、a+b+c+d=1、0≦x≦0.5、
の関係を満足すると共に、
上記層Bが、
(CreSi1-e)(CyN1-y)からなり、
CrおよびCの原子比を、夫々eおよびyとしたとき、
0.90≦e≦1.0、0≦y≦0.5、
の関係を満足するか、または、
(AlfSi1-f)(CzN1-z)からなり、
AlおよびCの原子比を、夫々fおよびzとしたとき、
0.90≦f≦1.0、0≦z≦0.5、
の関係を満足し、
前記層Aおよび層Bの厚みが各々2~100nmであり、夫々交互に積層したものであることを特徴とする。
0≦a≦0.10、0.10≦b≦0.50、0.50≦c≦0.90、0≦d≦0.05、a+b+c+d=1、0≦x≦0.5
(CreSi1-e)(CyN1-y)からなり、CrおよびCの原子比を、夫々eおよびyとしたとき、下記の関係を満足するか、
0.90≦e≦1.0、0≦y≦0.5
または、(AlfSi1-f)(CzN1-z)からなり、AlおよびCの原子比を、夫々fおよびzとしたとき、下記の関係を満足する。
0.90≦f≦1.0、0≦z≦0.5
層A1の組成:(Cr1-cAlc)N、層A1の厚み:qnm
即ち、規定の組成において、a=0、d=0、b=1-c、x=0
層B1の組成:CrN、層B1の厚み:rnm
即ち、規定の組成において、e=1、y=0
層A1中のAl原子数=(1/α)3×4×c
層A1中のCr原子数=(1/α)3×4×(1-c)
層B1中のCr原子数=(1/β)3×4
層A1と層B1のCr、Alの合計量に占めるAlの原子比=(1/α)3×4×c×q/[(1/α)3×4×c×q+(1/α)3×4×(1-c)×q+(1/β)3×4×r]
全圧力:0.5Pa以上、4Pa以下
印加電流(放電電流):100~200A
成膜時の基材温度:300℃以上、800℃以下
下記表1に示す組成の単層または積層型の皮膜を、AIP装置にて形成した。このとき、ターゲットは、層A、層Bの夫々の金属部分に相当するターゲットを使用した。また基材としては、三菱マテリアル株式会社製の微粒超硬合金HTi10と同じ成分を有する微粒WC-Co系の直径10mmの超硬合金製ボールを、表面鏡面仕上げして使用した。尚、下記表1の試験No.1~31については、皮膜を形成するに先立ち、厚み5μmのCrN膜を中間層として形成した。また試験No.32については、中間層を形成せずに基材表面に皮膜を直接形成した。

試験方法:ボールオンプレート型往復摺動
ボール:各種皮膜コーティング超硬合金製ボール
プレート:アルミナ板
垂直荷重:5N
摺動速度:0.1m/秒
摺動振幅:30mm
摺動距離:72m
温度:室温
圧子:先端の曲率半径が200μmのダイヤモンド圧子
荷重増加速度:100N/分
最大荷重:100N
圧子移動速度:10mm/分
温度:室温

下記表3に示す組成の積層型の皮膜を、実施例1と同様にして形成した。尚、下記表3の全ての例では、皮膜を形成するに先立ち、厚み5μmのCrN膜を中間層として形成した。尚、表3のNo.7の皮膜は表1のNo.22と同じである。また、表3のNo.10の皮膜は表1のNo.27、表3のNo.12の皮膜は表1のNo.28、表3のNo.14の皮膜は表1のNo.25、表3のNo.16の皮膜は表1のNo.30と、それぞれ同じである。
本出願は、2014年9月24日出願の日本特許出願(特願2014-193885)、2014年12月26日出願の日本特許出願(特願2014-266487)に基づくものであり、その内容はここに参照として取り込まれる。
Claims (9)
- 組成の異なる層Aと層Bが積層されてなる積層型硬質皮膜であって、
上記層Aが、
(TiaCrbAlcSid)(CxN1-x)からなり、
Ti、Cr、Al、SiおよびCの原子比を、夫々a、b、c、dおよびxとしたとき、0≦a≦0.10、0.10≦b≦0.50、0.50≦c≦0.90、0≦d≦0.05、a+b+c+d=1、0≦x≦0.5、
の関係を満足すると共に、
上記層Bが、
(CreSi1-e)(CyN1-y)からなり、
CrおよびCの原子比を、夫々eおよびyとしたとき、
0.90≦e≦1.0、0≦y≦0.5、
の関係を満足するか、または、
(AlfSi1-f)(CzN1-z)からなり、
AlおよびCの原子比を、夫々fおよびzとしたとき、
0.90≦f≦1.0、0≦z≦0.5、
の関係を満足し、
前記層Aおよび層Bの厚みが各々2~100nmであり、夫々交互に積層したものであることを特徴とする積層型硬質皮膜。 - 前記層Aと前記層BのTi、Cr、Al、Siの合計量に占めるAlの原子比が0.20~0.60の範囲にある請求項1に記載の積層型硬質皮膜。
- 前記層A中のTiの少なくとも一部をZrで置換したものである請求項1または2に記載の積層型硬質皮膜。
- 請求項1または2に記載の積層型硬質皮膜を基材表面に有する成形用金型。
- 請求項3に記載の積層型硬質皮膜を基材表面に有する成形用金型。
- 前記積層型硬質皮膜と前記基材の間に、CrNの中間層を厚み3~10μmで有するものである請求項4に記載の成形用金型。
- 前記積層型硬質皮膜と前記基材の間に、CrNの中間層を厚み3~10μmで有するものである請求項5に記載の成形用金型。
- 鉄鋼材料の熱間成形に用いられるものである請求項6に記載の成形用金型。
- 鉄鋼材料の熱間成形に用いられるものである請求項7に記載の成形用金型。
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP15845389.4A EP3199660A4 (en) | 2014-09-24 | 2015-09-15 | Laminated hard coating and molding die |
| US15/512,712 US20170291211A1 (en) | 2014-09-24 | 2015-09-15 | Laminated hard coating and molding die |
| CA2962195A CA2962195A1 (en) | 2014-09-24 | 2015-09-15 | Laminated hard coating and molding die |
| KR1020177007076A KR20170042705A (ko) | 2014-09-24 | 2015-09-15 | 적층형 경질 피막 및 성형용 금형 |
| CN201580050905.2A CN106715748A (zh) | 2014-09-24 | 2015-09-15 | 层叠型硬质皮膜和成形用模具 |
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2014-193885 | 2014-09-24 | ||
| JP2014193885 | 2014-09-24 | ||
| JP2014-266487 | 2014-12-26 | ||
| JP2014266487A JP6326367B2 (ja) | 2014-09-24 | 2014-12-26 | 積層型硬質皮膜および成形用金型 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2016047508A1 true WO2016047508A1 (ja) | 2016-03-31 |
Family
ID=55581035
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2015/076204 Ceased WO2016047508A1 (ja) | 2014-09-24 | 2015-09-15 | 積層型硬質皮膜および成形用金型 |
Country Status (1)
| Country | Link |
|---|---|
| WO (1) | WO2016047508A1 (ja) |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2007111815A (ja) * | 2005-10-19 | 2007-05-10 | Sumitomo Electric Hardmetal Corp | 表面被覆切削工具 |
| WO2007083361A1 (ja) * | 2006-01-18 | 2007-07-26 | Mitsubishi Heavy Industries, Ltd. | 耐固体粒子エロージョン性表面処理皮膜および回転機械 |
| JP2010115739A (ja) * | 2008-11-12 | 2010-05-27 | Sumitomo Electric Hardmetal Corp | 表面被覆切削工具 |
-
2015
- 2015-09-15 WO PCT/JP2015/076204 patent/WO2016047508A1/ja not_active Ceased
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2007111815A (ja) * | 2005-10-19 | 2007-05-10 | Sumitomo Electric Hardmetal Corp | 表面被覆切削工具 |
| WO2007083361A1 (ja) * | 2006-01-18 | 2007-07-26 | Mitsubishi Heavy Industries, Ltd. | 耐固体粒子エロージョン性表面処理皮膜および回転機械 |
| JP2010115739A (ja) * | 2008-11-12 | 2010-05-27 | Sumitomo Electric Hardmetal Corp | 表面被覆切削工具 |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP3199660A4 * |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP4373897B2 (ja) | 硬質皮膜被覆部材及びその被覆方法 | |
| JP6222675B2 (ja) | 表面被覆切削工具、およびその製造方法 | |
| JP6491031B2 (ja) | 積層型硬質皮膜および切削工具 | |
| JP4714186B2 (ja) | 被覆切削工具 | |
| JP2013233652A (ja) | 表面被覆切削工具 | |
| JP2009178822A (ja) | 切削工具用硬質皮膜 | |
| JP5395454B2 (ja) | 表面被覆切削工具 | |
| KR100816175B1 (ko) | 경질 피막 및 경질 피막 형성용 스퍼터링 타겟재 | |
| CN106029940B (zh) | 硬质皮膜及其形成方法、和钢板热成型用模具 | |
| JP5681093B2 (ja) | 多層硬質皮膜 | |
| WO2012057000A1 (ja) | 硬質皮膜形成部材および硬質皮膜の形成方法 | |
| JP2004351586A (ja) | 切削工具用硬質皮膜 | |
| JP6326367B2 (ja) | 積層型硬質皮膜および成形用金型 | |
| JP4441494B2 (ja) | 硬質皮膜被覆部材 | |
| KR101727420B1 (ko) | 내마모성이 우수한 적층 피막 | |
| JP6273161B2 (ja) | 耐摩耗性に優れた積層皮膜 | |
| JP2010105137A (ja) | 表面被覆切削工具 | |
| WO2016125396A1 (ja) | 硬質皮膜 | |
| WO2017159030A1 (ja) | 硬質皮膜及び硬質皮膜被覆部材 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 15845389 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 20177007076 Country of ref document: KR Kind code of ref document: A |
|
| ENP | Entry into the national phase |
Ref document number: 2962195 Country of ref document: CA |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 15512712 Country of ref document: US |
|
| REEP | Request for entry into the european phase |
Ref document number: 2015845389 Country of ref document: EP |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2015845389 Country of ref document: EP |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |