WO2016132986A1 - 包装充填装置 - Google Patents
包装充填装置 Download PDFInfo
- Publication number
- WO2016132986A1 WO2016132986A1 PCT/JP2016/053934 JP2016053934W WO2016132986A1 WO 2016132986 A1 WO2016132986 A1 WO 2016132986A1 JP 2016053934 W JP2016053934 W JP 2016053934W WO 2016132986 A1 WO2016132986 A1 WO 2016132986A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- packaging
- anvil
- filling apparatus
- strip
- packaging material
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B9/00—Enclosing successive articles, or quantities of material, e.g. liquids or semiliquids, in flat, folded, or tubular webs of flexible sheet material; Subdividing filled flexible tubes to form packages
- B65B9/10—Enclosing successive articles, or quantities of material, in preformed tubular webs, or in webs formed into tubes around filling nozzles, e.g. extruded tubular webs
- B65B9/20—Enclosing successive articles, or quantities of material, in preformed tubular webs, or in webs formed into tubes around filling nozzles, e.g. extruded tubular webs the webs being formed into tubes in situ around the filling nozzles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C65/00—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor
- B29C65/02—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure
- B29C65/08—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using ultrasonic vibrations
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C65/00—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor
- B29C65/74—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by welding and severing, or by joining and severing, the severing being performed in the area to be joined, next to the area to be joined, in the joint area or next to the joint area
- B29C65/745—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by welding and severing, or by joining and severing, the severing being performed in the area to be joined, next to the area to be joined, in the joint area or next to the joint area using a single unit having both a severing tool and a welding tool
- B29C65/7451—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by welding and severing, or by joining and severing, the severing being performed in the area to be joined, next to the area to be joined, in the joint area or next to the joint area using a single unit having both a severing tool and a welding tool the severing tool and the welding tool being movable with respect to one-another
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/001—Joining in special atmospheres
- B29C66/0012—Joining in special atmospheres characterised by the type of environment
- B29C66/0018—Joining in special atmospheres characterised by the type of environment being sterile
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/01—General aspects dealing with the joint area or with the area to be joined
- B29C66/05—Particular design of joint configurations
- B29C66/10—Particular design of joint configurations particular design of the joint cross-sections
- B29C66/11—Joint cross-sections comprising a single joint-segment, i.e. one of the parts to be joined comprising a single joint-segment in the joint cross-section
- B29C66/112—Single lapped joints
- B29C66/1122—Single lap to lap joints, i.e. overlap joints
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/01—General aspects dealing with the joint area or with the area to be joined
- B29C66/346—Making joints having variable thicknesses in the joint area, e.g. by using jaws having an adapted configuration
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/40—General aspects of joining substantially flat articles, e.g. plates, sheets or web-like materials; Making flat seams in tubular or hollow articles; Joining single elements to substantially flat surfaces
- B29C66/41—Joining substantially flat articles ; Making flat seams in tubular or hollow articles
- B29C66/43—Joining a relatively small portion of the surface of said articles
- B29C66/431—Joining the articles to themselves
- B29C66/4312—Joining the articles to themselves for making flat seams in tubular or hollow articles, e.g. transversal seams
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/70—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material
- B29C66/71—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the composition of the plastics material of the parts to be joined
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/70—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material
- B29C66/72—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined
- B29C66/723—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined being multi-layered
- B29C66/7232—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined being multi-layered comprising a non-plastics layer
- B29C66/72327—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined being multi-layered comprising a non-plastics layer consisting of natural products or their composites, not provided for in B29C66/72321 - B29C66/72324
- B29C66/72328—Paper
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/70—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material
- B29C66/73—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset
- B29C66/739—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset
- B29C66/7392—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of at least one of the parts being a thermoplastic
- B29C66/73921—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the intensive physical properties of the material of the parts to be joined, by the optical properties of the material of the parts to be joined, by the extensive physical properties of the parts to be joined, by the state of the material of the parts to be joined or by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of the parts to be joined being a thermoplastic or a thermoset characterised by the material of at least one of the parts being a thermoplastic characterised by the materials of both parts being thermoplastics
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/81—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps
- B29C66/814—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps
- B29C66/8141—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined
- B29C66/81411—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined characterised by its cross-section, e.g. transversal or longitudinal, being non-flat
- B29C66/81415—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined characterised by its cross-section, e.g. transversal or longitudinal, being non-flat being bevelled
- B29C66/81419—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined characterised by its cross-section, e.g. transversal or longitudinal, being non-flat being bevelled and flat
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/81—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps
- B29C66/814—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps
- B29C66/8141—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined
- B29C66/81411—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined characterised by its cross-section, e.g. transversal or longitudinal, being non-flat
- B29C66/81425—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined characterised by its cross-section, e.g. transversal or longitudinal, being non-flat being stepped, e.g. comprising a shoulder
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/81—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps
- B29C66/814—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps
- B29C66/8141—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined
- B29C66/81427—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined comprising a single ridge, e.g. for making a weakening line; comprising a single tooth
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/81—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps
- B29C66/814—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps
- B29C66/8141—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined
- B29C66/81431—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined comprising a single cavity, e.g. a groove
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/81—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps
- B29C66/814—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps
- B29C66/8141—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined
- B29C66/81433—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined being toothed, i.e. comprising several teeth or pins, or being patterned
- B29C66/81435—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the design of the pressing elements, e.g. of the welding jaws or clamps characterised by the surface geometry of the part of the pressing elements, e.g. welding jaws or clamps, coming into contact with the parts to be joined being toothed, i.e. comprising several teeth or pins, or being patterned comprising several parallel ridges, e.g. for crimping
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/81—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps
- B29C66/816—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the mounting of the pressing elements, e.g. of the welding jaws or clamps
- B29C66/8167—Quick change joining tools or surfaces
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/81—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps
- B29C66/818—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the cooling constructional aspects, or by the thermal or electrical insulating or conducting constructional aspects of the welding jaws or of the clamps ; comprising means for compensating for the thermal expansion of the welding jaws or of the clamps
- B29C66/8181—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the cooling constructional aspects, or by the thermal or electrical insulating or conducting constructional aspects of the welding jaws or of the clamps ; comprising means for compensating for the thermal expansion of the welding jaws or of the clamps characterised by the cooling constructional aspects
- B29C66/81811—General aspects of the pressing elements, i.e. the elements applying pressure on the parts to be joined in the area to be joined, e.g. the welding jaws or clamps characterised by the cooling constructional aspects, or by the thermal or electrical insulating or conducting constructional aspects of the welding jaws or of the clamps ; comprising means for compensating for the thermal expansion of the welding jaws or of the clamps characterised by the cooling constructional aspects of the welding jaws
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/83—General aspects of machine operations or constructions and parts thereof characterised by the movement of the joining or pressing tools
- B29C66/832—Reciprocating joining or pressing tools
- B29C66/8322—Joining or pressing tools reciprocating along one axis
- B29C66/83221—Joining or pressing tools reciprocating along one axis cooperating reciprocating tools, each tool reciprocating along one axis
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/80—General aspects of machine operations or constructions and parts thereof
- B29C66/84—Specific machine types or machines suitable for specific applications
- B29C66/849—Packaging machines
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B51/00—Devices for, or methods of, sealing or securing package folds or closures; Devices for gathering or twisting wrappers, or necks of bags
- B65B51/10—Applying or generating heat or pressure or combinations thereof
- B65B51/22—Applying or generating heat or pressure or combinations thereof by friction or ultrasonic or high-frequency electrical means
- B65B51/225—Applying or generating heat or pressure or combinations thereof by friction or ultrasonic or high-frequency electrical means by ultrasonic welding
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B51/00—Devices for, or methods of, sealing or securing package folds or closures; Devices for gathering or twisting wrappers, or necks of bags
- B65B51/10—Applying or generating heat or pressure or combinations thereof
- B65B51/26—Devices specially adapted for producing transverse or longitudinal seams in webs or tubes
- B65B51/30—Devices, e.g. jaws, for applying pressure and heat, e.g. for subdividing filled tubes
- B65B51/303—Devices, e.g. jaws, for applying pressure and heat, e.g. for subdividing filled tubes reciprocating along only one axis
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B55/00—Preserving, protecting or purifying packages or package contents in association with packaging
- B65B55/02—Sterilising, e.g. of complete packages
- B65B55/04—Sterilising wrappers or receptacles prior to, or during, packaging
- B65B55/10—Sterilising wrappers or receptacles prior to, or during, packaging by liquids or gases
- B65B55/103—Sterilising flat or tubular webs
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B61/00—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages
- B65B61/18—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for making package-opening or unpacking elements
- B65B61/182—Auxiliary devices, not otherwise provided for, for operating on sheets, blanks, webs, binding material, containers or packages for making package-opening or unpacking elements by applying tear-strips or tear-tapes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C2795/00—Printing on articles made from plastics or substances in a plastic state
- B29C2795/002—Printing on articles made from plastics or substances in a plastic state before shaping
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C65/00—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor
- B29C65/02—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure
- B29C65/10—Joining or sealing of preformed parts, e.g. welding of plastics materials; Apparatus therefor by heating, with or without pressure using hot gases (e.g. combustion gases) or flames coming in contact with at least one of the parts to be joined
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/01—General aspects dealing with the joint area or with the area to be joined
- B29C66/02—Preparation of the material, in the area to be joined, prior to joining or welding
- B29C66/024—Thermal pre-treatments
- B29C66/0242—Heating, or preheating, e.g. drying
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/40—General aspects of joining substantially flat articles, e.g. plates, sheets or web-like materials; Making flat seams in tubular or hollow articles; Joining single elements to substantially flat surfaces
- B29C66/41—Joining substantially flat articles ; Making flat seams in tubular or hollow articles
- B29C66/43—Joining a relatively small portion of the surface of said articles
- B29C66/432—Joining a relatively small portion of the surface of said articles for making tubular articles or closed loops, e.g. by joining several sheets ; for making hollow articles or hollow preforms
- B29C66/4322—Joining a relatively small portion of the surface of said articles for making tubular articles or closed loops, e.g. by joining several sheets ; for making hollow articles or hollow preforms by joining a single sheet to itself
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/70—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material
- B29C66/72—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined
- B29C66/723—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined being multi-layered
- B29C66/7232—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined being multi-layered comprising a non-plastics layer
- B29C66/72321—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined being multi-layered comprising a non-plastics layer consisting of metals or their alloys
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/70—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material
- B29C66/72—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined
- B29C66/723—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined being multi-layered
- B29C66/7234—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined being multi-layered comprising a barrier layer
- B29C66/72341—General aspects of processes or apparatus for joining preformed parts characterised by the composition, physical properties or the structure of the material of the parts to be joined; Joining with non-plastics material characterised by the structure of the material of the parts to be joined being multi-layered comprising a barrier layer for gases
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/90—Measuring or controlling the joining process
- B29C66/94—Measuring or controlling the joining process by measuring or controlling the time
- B29C66/949—Measuring or controlling the joining process by measuring or controlling the time characterised by specific time values or ranges
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/90—Measuring or controlling the joining process
- B29C66/95—Measuring or controlling the joining process by measuring or controlling specific variables not covered by groups B29C66/91 - B29C66/94
- B29C66/951—Measuring or controlling the joining process by measuring or controlling specific variables not covered by groups B29C66/91 - B29C66/94 by measuring or controlling the vibration frequency and/or the vibration amplitude of vibrating joining tools, e.g. of ultrasonic welding tools
- B29C66/9513—Measuring or controlling the joining process by measuring or controlling specific variables not covered by groups B29C66/91 - B29C66/94 by measuring or controlling the vibration frequency and/or the vibration amplitude of vibrating joining tools, e.g. of ultrasonic welding tools characterised by specific vibration frequency values or ranges
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29C—SHAPING OR JOINING OF PLASTICS; SHAPING OF MATERIAL IN A PLASTIC STATE, NOT OTHERWISE PROVIDED FOR; AFTER-TREATMENT OF THE SHAPED PRODUCTS, e.g. REPAIRING
- B29C66/00—General aspects of processes or apparatus for joining preformed parts
- B29C66/90—Measuring or controlling the joining process
- B29C66/95—Measuring or controlling the joining process by measuring or controlling specific variables not covered by groups B29C66/91 - B29C66/94
- B29C66/951—Measuring or controlling the joining process by measuring or controlling specific variables not covered by groups B29C66/91 - B29C66/94 by measuring or controlling the vibration frequency and/or the vibration amplitude of vibrating joining tools, e.g. of ultrasonic welding tools
- B29C66/9517—Measuring or controlling the joining process by measuring or controlling specific variables not covered by groups B29C66/91 - B29C66/94 by measuring or controlling the vibration frequency and/or the vibration amplitude of vibrating joining tools, e.g. of ultrasonic welding tools characterised by specific vibration amplitude values or ranges
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29K—INDEXING SCHEME ASSOCIATED WITH SUBCLASSES B29B, B29C OR B29D, RELATING TO MOULDING MATERIALS OR TO MATERIALS FOR MOULDS, REINFORCEMENTS, FILLERS OR PREFORMED PARTS, e.g. INSERTS
- B29K2705/00—Use of metals, their alloys or their compounds, for preformed parts, e.g. for inserts
- B29K2705/02—Aluminium
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29L—INDEXING SCHEME ASSOCIATED WITH SUBCLASS B29C, RELATING TO PARTICULAR ARTICLES
- B29L2031/00—Other particular articles
- B29L2031/712—Containers; Packaging elements or accessories, Packages
- B29L2031/7162—Boxes, cartons, cases
- B29L2031/7166—Cartons of the fruit juice or milk type, i.e. containers of polygonal cross sections formed by folding blanks into a tubular body with end-closing or contents-supporting elements, e.g. gable type containers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B55/00—Preserving, protecting or purifying packages or package contents in association with packaging
- B65B55/02—Sterilising, e.g. of complete packages
- B65B55/04—Sterilising wrappers or receptacles prior to, or during, packaging
- B65B55/08—Sterilising wrappers or receptacles prior to, or during, packaging by irradiation
Definitions
- the present invention relates to a packaging filling apparatus for filling a packaging material with a fluid food or the like.
- a packaging container is formed by sealing with a seal, an ultrasonic seal, or the like.
- a packaging laminate material is formed into a tube shape, sealed in the longitudinal direction (longitudinal direction) by a longitudinal sealing device, and then filled with liquid food in the tubular packaging laminate material and then laterally sealed.
- the apparatus is sealed and cut in the lateral direction to form a pillow-shaped preformed container, and the preformed container is further formed into a final shape to complete a packaging container.
- the horizontal sealing device in addition to a device that performs heat sealing using a heater, an inductor, or the like, a device that performs ultrasonic sealing using ultrasonic waves is known (see Patent Document 1).
- An object of the present invention is to provide a packaging and filling apparatus capable of realizing a good seal by ultrasonic sealing.
- a packaging and filling apparatus is a packaging and filling apparatus that forms a packaging container that contains a flowable food in a band-shaped packaging material and that contains the flowable food, and an ultrasonic supply unit that supplies ultrasonic waves And an anvil which is a receiving jig, the band-shaped packaging material is sandwiched between the ultrasonic supply surface of the ultrasonic supply section and the receiving surface of the anvil, and the band-shaped packaging material sandwiched between A sealing device that seals the belt-shaped packaging material by applying sound waves, and the receiving surface of the anvil has a smooth corner in a region adjacent to the contact portion that contacts the belt-shaped packaging material when sealing; It is characterized by a certain smooth shape.
- the smooth shape may be a smooth shape in which the apex angle of the corner portion is in the range of 155 to 175 degrees.
- the corner may be chamfered in the smooth shape.
- a predetermined area that is a part of the receiving surface of the anvil may be the smooth shape.
- the predetermined area may be two areas that are separated from each other by a predetermined distance from the center of the receiving surface of the anvil and sandwich an edge of the strip-shaped packaging material.
- the sealing device may seal the strip-shaped packaging material in a direction orthogonal to the longitudinal direction of the strip-shaped packaging material.
- the receiving surface of the anvil has a shape without an angular portion in the region adjacent to the contact portion that contacts the belt-shaped packaging material at the time of sealing, a good seal is realized by ultrasonic sealing. can do.
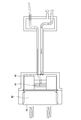
- FIG. 1 It is a perspective view which shows the outline
- the strip-shaped packaging laminate material 1 is supplied to the packaging filling device in a reel state.
- the packaging laminate material 1 is composed of a paper substrate and a flexible laminate in which polyethylene resin is laminated on both sides of the paper substrate, and an aluminum foil or gas barrier property between the paper substrate and the film as necessary.
- a barrier layer made of a resin or the like is formed, and characters and patterns are printed in advance on a portion corresponding to the surface of the packaging container 14.
- the fed packaging laminate material 1 is continuously conveyed by a feeding device as a conveying means, is sent to a strip adhering device 3 through a bending roller, a damper roller, and the like, and is fed to one edge of the packaging laminate material 1 by the strip adhering device.
- a strip 2 is attached along the part.
- the packing laminated material 1 is attached with a pull tab by a pull tab attaching device as necessary.
- the packaging laminated material 1 is sent to the sterilization tank 4 and sterilized with a sterilization liquid such as hydrogen peroxide in the sterilization tank 4.
- sterilization may be performed by irradiating an electron beam.
- the packaging laminate material 1 is sent to the upper chamber 30, dried by the air knife 33 in the upper chamber 30, and then sent into the aseptic room 16.
- the packaging laminated material 1 is gradually deformed by the forming ring 37 or the like to be formed into a tube shape.
- the packaging laminate material 1 is preheated by hot air from the preheating means of the longitudinal seal device 8, sealed in the longitudinal direction, and the fluid food supplied via the filling pipe 7 is converted into the tubular packaging laminate material 1. Filled in.
- the tubular packaging laminate material 1 filled with the fluid food is guided by a roller, sent to the horizontal sealing device 10, and sandwiched and sealed in the horizontal direction.
- the horizontally sealed packaging laminate material is cut with a cutting blade or the like to form a pillow-shaped preformed container 13.
- the preforming container 13 is conveyed by the final shaping
- the horizontal sealing device 10 of the present embodiment seals the tubular packaging laminate material 1 by ultrasonic sealing.
- the ultrasonic horn 40 that supplies ultrasonic waves and the anvil 50 that is a receiving jig are opposed to each other, and the packaging laminate material 1 is passed between them.
- the packaging laminate material 1 is temporarily stopped, and the packaging laminate material 1 is sandwiched between the anvil 50 and the ultrasonic horn 40.
- the packaging laminate material 1 is laterally sealed by two adjacent seal portions 13A and 13A by ultrasonic waves from the ultrasonic horn 40.
- the cutting part 13B between the two sealing parts 13A and 13A that are laterally sealed is cut by the cutting blade 60 to form the pillow-shaped preformed container 13.
- a piezoelectric element 44 that expands and contracts when a voltage is applied is provided on the opposite side of the ultrasonic supply surface 42 of the ultrasonic horn 40.
- An air chamber 46 filled with compressed air is provided on the opposite side of the ultrasonic supply surface 42 of the ultrasonic horn 40 including the piezoelectric element 44. The pressure in the air chamber 46 is adjusted to cool.
- the lateral width of the packaging laminate material 1 to be laterally sealed is, for example, 60 to 160 mm.
- the ultrasonic supply surface 42 of the ultrasonic horn 40 has, for example, a rectangular shape with a width of 150 to 200 mm and a length of 10 to 20 mm.
- the receiving surface 52 of the anvil 50 which is a receiving jig of the ultrasonic horn 40, has substantially the same size and shape as the ultrasonic supply surface 42 of the ultrasonic horn 40.
- the receiving surface 52 is 150 to 200 mm wide and 10 to 20 mm long. It has a rectangular shape.
- the shape of the region sandwiching the edge of the packaging laminate material 1 is partially changed on the receiving surface 52 of the anvil 50 that is a receiving jig.
- the edge of the packaging laminate material 1 is sandwiched between regions P and Q at a predetermined distance from the center of the receiving surface 52 of the anvil 50.
- the shape of the receiving surface 52 of the anvil 50 in the regions P and Q is different from the shape of the receiving surface 52 of the anvil 50 in other regions.
- the regions P and Q are at a distance of, for example, 30 to 80 mm from the center of the anvil 50, and the length thereof is, for example, 10 to 20 mm.
- a concave portion 54 that accommodates an overlap portion of the packaging laminate material 1 is formed at the center of the receiving surface 52 of the anvil 50 that is a receiving jig.
- the packaging laminated material 1 is sandwiched between the ultrasonic horn 40 and the anvil 50.
- An ultrasonic wave having an optimum frequency and amplitude is supplied from the ultrasonic horn 40 to the packaging laminate material 1 to be sealed, and the packaging laminate material 1 is laterally sealed.
- an ultrasonic wave having a frequency of 15 to 40 KHz and an amplitude of 10 to 40 ⁇ m is supplied from the ultrasonic horn 40 for a time of 100 to 500 msec.
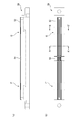
- FIG. 6A is a front view of the anvil 50
- FIG. 6B is a plan view of the anvil 50
- 7 is a cross-sectional view of the anvil 50 taken along the line AA ′
- FIG. 8 is a cross-sectional view of the anvil 50 taken along the line BB ′.
- a rectangular receiving surface 52 is formed on the anvil 50 of the lateral sealing device 10 of the packaging filling device.
- the shape of the region that sandwiches the edge of the packaging laminate material 1 is partially changed. As shown in FIG. 6, the shapes in the regions P and Q that are a predetermined distance from the center of the receiving surface 52 of the anvil 50 are partially changed.
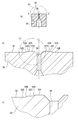
- FIG. 7 shows a basic cross-sectional shape of the receiving surface 52 of the anvil 50.
- FIG. 8 is a cross-sectional shape of the changed portion in the regions P and Q of the receiving surface 52 of the anvil 50.
- FIGS. 7A and 8A are sectional views of the entire anvil 50.
- FIGS. 7B and 8B are enlarged portions of FIGS. 7A and 8A.
- 7 (c) and 8 (c) are further enlarged partial sectional views of FIGS. 7 (b) and 8 (b).
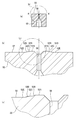
- contact portions 52A that directly contact the packaging laminate material 1 are provided on the left and right sides of the cutting blade passage hole 56 of the cutting blade 60.
- the packaging laminate material 1 is sandwiched between the contact portion 52A and the ultrasonic horn 40, and the portion in contact with the contact portion 52A is laterally sealed by ultrasonic waves.
- the basic cross-sectional shape of the receiving surface 52 of the anvil 50 is provided with a flat portion 52C through an inclined portion 52B at an adjacent portion on the opposite side of the cutting blade passage hole 56 side of the contact portion 52A. Further, a flat portion 52E is provided through an inclined portion 52D.
- the cross-sectional shape of the receiving surface 52 of the anvil 50 in the regions P and Q has an inclined portion 52 ⁇ / b> B in an adjacent portion opposite to the cutting blade passage hole 56 side of the contact portion 52 ⁇ / b> A.
- a flat part 52C is provided, and further a flat part 52E is provided via an inclined part 52D.
- the flat portion 52C has a narrow width
- the inclined portion 52D has a wide width
- the inclination is gentle compared to the basic cross-sectional shape.
- the basic cross-sectional shape is shown by a broken line for comparison.
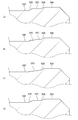
- FIG. 9 is an enlarged partial sectional view of the anvil 50.
- FIG. 9A corresponds to FIG. 7 and shows a basic cross-sectional shape of the receiving surface 52 of the anvil 50.
- the width of the contact portion 52A of the receiving surface 52 of the anvil 50 is, for example, 1.0 mm.
- the flat part 52C is parallel to the surface of the contact part 52A, and is 0.10 mm lower than the contact part 52A, for example.
- the width of the flat part 52C is 1.0 mm, for example.
- the inclined portion 52B is located between the contact surface 52A and the flat portion 52C.
- the inclination angle of the inclined portion 52B is, for example, 30 degrees, and the width of the inclined portion 52B is, for example, 0.10 mm.
- the flat part 52E is parallel to the surfaces of the contact part 52A and the flat part 52C, and is, for example, 0.10 mm lower than the flat part 52C.
- the inclined part 52D is positioned between the flat part 52C and the flat part 52E. is doing.
- the inclination angle of the inclined part 52D is, for example, 30 degrees.
- the width of the inclined portion 52D is, for example, 0.10 mm
- FIG. 9B corresponds to FIG. 8 and shows a cross-sectional shape in the regions P and Q of the receiving surface 52 of the anvil 50.
- the basic cross-sectional shape is indicated by a broken line.
- the width of the contact portion 52A of the receiving surface 52 of the anvil 50 is, for example, 0.5 to 3.0 mm.
- the flat part 52C is parallel to the surface of the contact part 52A and is lower by, for example, 0.05 to 0.20 mm than the contact part 52A.
- the width of the flat part 52C is shorter than the basic cross-sectional shape, for example, 0.5 to 1.5 mm.
- the inclined portion 52B is located between the contact surface 52A and the flat portion 52C.
- the inclination angle of the inclined portion 52B is smaller than the basic cross-sectional shape and is gentle, for example, 15 to 25 degrees, and the width of the inclined portion 52B is, for example, 0.05 to 0.20 mm.
- the flat part 52E is parallel to the surfaces of the contact part 52A and the flat part 52C, and is lower by 0.05 to 0.20 mm, for example, than the flat part 52C.
- the inclined part 52D is located between the flat part 52C and the flat part 52E.
- the inclination angle of the inclined portion 52D is gentler than the basic cross-sectional shape, and is, for example, 15 to 25 degrees.
- the width of the inclined portion 52D is, for example, 0.10 to 0.20 mm.
- the edge of the packaging laminate material 1 is sandwiched.
- the packaging laminate material 1 is bent and sandwiched at the edge of the packaging laminate material 1, bulky polyethylene is likely to be generated during horizontal sealing. When bulk polyethylene is generated, minute defects are generated by pinholes.
- the width of the flat portion 52C is made shorter than the basic cross-sectional shape, and the inclination angle of the inclined portion 52D is made gentler than the basic cross-sectional shape, whereby the contact portion 52A of the receiving surface 52 of the anvil 50 is formed.
- Generation of lump-like polyethylene is prevented at the time of transverse sealing at the edge of the packaging laminate material 1 so that there is no angular portion in the adjacent region.
- the shape of the adjacent portion of the contact portion 52A of the receiving surface 52 of the anvil 50 is not limited to the shape of FIG. 9 (b) as long as there is no angular portion.
- the flat portion 52E may be formed from the contact surface 52A via the inclined portions 52B and 52D without providing the flat portion 52C.
- the basic cross-sectional shape is indicated by a broken line. Since there is no flat part 52C, the inclined part 52D is located between the inclined part 52B and the flat part 52E.
- the inclination angle of the inclined portion 52D is more gradual than the basic cross-sectional shape, for example, 10 to 20 degrees.
- the width of the inclined portion 52D is, for example, 1.0 to 3.0 mm.
- FIG. 9D a cross-sectional shape as shown in FIG.
- the basic cross-sectional shape is indicated by a broken line.
- the overall cross-sectional shape is similar to the basic cross-sectional shape, and the inclined portion 52B, the flat portion 52C, the inclined portion 52D, and the flat portion 52E are adjacent to the contact portion 52A adjacent to the cutting blade passage hole 56 side.
- the corner portion between the contact portion 52A and the inclined portion 52B and the corner portion between the flat portion 52C and the inclined portion 52D are rounded.
- the corner portion between the contact portion 52A and the inclined portion 52B is, for example, an R chamfer having a diameter of 5.0 to 10.0 mm, and the corner portion between the flat portion 52C and the inclined portion 52D, for example, a diameter of 5.0 R chamfering of ⁇ 10.0mm.
- the cross-sectional shapes of the anvils are different in the regions P and Q that are partial regions of the anvil, but the present invention is not limited to this.
- the cross-sectional shape of the anvil may be different in regions other than the anvil regions P and Q.
- the cross-sectional shape of the anvil may be a cross-sectional shape such as regions P and Q.
- the present invention is applied to the horizontal seal.
- the present invention may be applied to a seal at another location such as a vertical seal.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Composite Materials (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Health & Medical Sciences (AREA)
- Toxicology (AREA)
- Package Closures (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
Abstract
超音波シールにより良好なシールを実現することができる包装充填装置を提供する。帯状の包装材料に流動性食品を充填し、流動性食品を収容する包装容器を形成する包装充填装置であって、超音波を供給する超音波供給部と、受け治具であるアンビルとを有し、超音波供給部の超音波供給面とアンビルの受け面とで帯状の包装材料を挟持し、挟持された帯状の包装材料に超音波を印加して、帯状の包装材料をシールするシール装置を有し、アンビルの前記受け面が、シール時に前記帯状の包装材料と接触する接触部に隣接する領域の角張った部分がない滑らかな形状である。
Description
本発明は、包装材料に流動性食品等を充填する包装充填装置に関する。
発酵乳飲料、牛乳、ミネラルウォーター、茶、ジュース、スープ、アルコール類等の流動性食品を収容する包装容器を製造する場合、ウェブ状(帯状)の包装積層材料が使用され、包装積層材料がヒートシール、超音波シール等によってシールされることにより、包装容器が形成される。例えば、包装充填装置において、包装積層材料をチューブ状に成形し、縦シール装置によって長手方向(縦方向)にシールした後、チューブ状の包装積層材料の中に液体食品を充填しながら、横シール装置によって横方向にシールして切断し、枕状の予備成形容器を形成し、予備成形容器を更に最終形状に成形して包装容器を完成させる。
横シール装置では、ヒータ、インダクタ等を利用してヒートシールを行うもののほかに、超音波を利用して超音波シールを行うものが知られている(特許文献1参照)。
本発明の目的は、超音波シールにより良好なシールを実現することができる包装充填装置を提供することにある。
本発明の一態様による包装充填装置は、帯状の包装材料に流動性食品を充填し、流動性食品を収容する包装容器を形成する包装充填装置であって、超音波を供給する超音波供給部と、受け治具であるアンビルとを有し、前記超音波供給部の超音波供給面と前記アンビルの受け面とで前記帯状の包装材料を挟持し、挟持された前記帯状の包装材料に超音波を印加して、前記帯状の包装材料をシールするシール装置を有し、前記アンビルの前記受け面が、シール時に前記帯状の包装材料と接触する接触部に隣接する領域における角部が滑らかである滑らか形状であることを特徴とする。
上述した包装充填装置において、前記滑らか形状は、前記角部の頂角が155~175度の範囲内である滑らか形状であるようにしてもよい。
上述した包装充填装置において、前記滑らか形状は、前記角部が面取りされているようにしてもよい。
上述した包装充填装置において、前記アンビルの前記受け面の一部である所定領域が前記滑らか形状であるようにしてもよい。
上述した包装充填装置において、前記所定領域は、前記アンビルの前記受け面の中央からそれぞれ所定距離離れ、前記帯状の包装材料の縁部を挟持する2つの領域であるようにしてもよい。
上述した包装充填装置において、前記シール装置は、前記帯状の包装材料の長手方向に直交する方向で、前記帯状の包装材料をシールするようにしてもよい。
以上の通り、本発明によれば、アンビルの受け面がシール時に帯状の包装材料と接触する接触部に隣接する領域に角張った部分がない形状であるので、超音波シールにより良好なシールを実現することができる。
[一実施形態]
本発明の一実施形態による包装充填装置について図面を用いて説明する。
本発明の一実施形態による包装充填装置について図面を用いて説明する。
(包装充填装置の概要)
まず、図1を用いて包装充填装置の概要について説明する。
まず、図1を用いて包装充填装置の概要について説明する。
帯状の包装積層材料1は、リールの状態で包装充填装置に供給される。包装積層材料1は、紙基材、及び紙基材の両面にポリエチレン樹脂が積層された可撓性の積層体から成り、必要に応じて紙基材とフィルムとの間にアルミニウム箔、ガスバリヤ性樹脂等から成るバリヤ層が形成され、包装容器14の表面に相当する部分にあらかじめ文字や模様などが印刷されている。
繰り出された包装積層材料1は、搬送手段としての送り装置によって連続的に搬送され、ベンディングローラ、ダンパローラ等を経て、ストリップ付着装置3に送られ、ストリップ付着装置によって包装積層材料1の一方の縁部に沿ってストリップ2が付着される。
続いて、包装積層材料1は、必要に応じて、プルタブ付着装置によってプルタブが付着されている。包装積層材料1は、殺菌槽4に送られ、殺菌槽4において過酸化水素等の殺菌液によって殺菌される。
なお、過酸化水素等の殺菌液を用いて殺菌する代わりに、電子線を照射して滅菌してもよい。
続いて、包装積層材料1は、アッパーチャンバ30に送られ、アッパーチャンバ30内のエアナイフ33によって乾燥させられた後、無菌室16の室内に送られる。
続いて、包装積層材料1は、フォーミングリング37等によって徐々に変形させられてチューブ状の形状に形成される。
続いて、包装積層材料1は、縦シール装置8の予熱手段からのホットエアーによって予熱されて、縦方向にシールされ、充填パイプ7を介して供給された流動性食品がチューブ状包装積層材料1内に充填される。
続いて、流動性食品が充填されたチューブ状包装積層材料1は、ローラによって案内され、横シール装置10に送られ、挟まれて横方向にシールされる。横シールされた包装積層材料は、切断刃などで切断されて枕状の予備成形容器13が形成される。そして、予備成形容器13は、最終成形搬送装置15によって搬送されて最終の形状に成形され、流動性食品を収容する包装容器14が完成する。
(包装充填装置の横シール装置)
次に、図2を用いて包装充填装置の横シール装置10について説明する。
次に、図2を用いて包装充填装置の横シール装置10について説明する。
本実施形態の横シール装置10は、超音波シールによりチューブ状包装積層材料1をシールする。超音波を供給する超音波ホーン40と、受け治具であるアンビル50とを対向させ、それらの間に包装積層材料1を通過させる。
横シール時には、包装積層材料1を一時的に停止させ、包装積層材料1をアンビル50と超音波ホーン40とで挟持する。超音波ホーン40からの超音波により包装積層材料1を近接する2個所のシール部13A、13Aで横シールする。横シールした2個所のシール部13A、13A間の切断部13Bを切断刃60により切断し、枕状の予備成形容器13を形成する。
次に、図3を用いて、横シール装置10の超音波ホーン40の詳細について説明する。
超音波ホーン40の超音波供給面42の反対側には、電圧を加えると伸び縮みするピエゾ素子44が設けられている。ピエゾ素子44を含む超音波ホーン40の超音波供給面42の反対側には、圧縮空気が封入されたエアー室46が設けられている。エアー室46の圧力を調整して、冷却する。
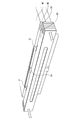
次に、図4及び図5を用いて、横シール装置10の要部について説明する。
本実施形態の場合、横シールする包装積層材料1の横幅は、例えば、60~160mmである。
超音波ホーン40の超音波供給面42は、例えば、横150~200mm、縦10~20mmの矩形形状である。
超音波ホーン40の受け治具であるアンビル50の受け面52は、超音波ホーン40の超音波供給面42とほぼ同じ大きさ及び形状であり、例えば、横150~200mm、縦10~20mmの矩形形状である。
本実施形態の横シール装置10では、受け治具であるアンビル50の受け面52において、包装積層材料1の縁部を挟持する領域の形状を部分的に変更している。
図4及び図5に示すように、包装積層材料1の縁部は、アンビル50の受け面52の中央から所定距離にある領域P、Qで挟持する。この領域P、Qのアンビル50の受け面52の形状を、その他の領域のアンビル50の受け面52の形状とは異ならしている。
領域P、Qは、アンビル50の中央から、例えば、30~80mmの距離にあり、その長さは、例えば、10~20mmである。
本実施形態の横シール装置10では、受け治具であるアンビル50の受け面52の中央には、包装積層材料1のオーバラップ部分を収容する凹部54が形成されている。包装積層材料1を超音波ホーン40とアンビル50で挟持したときに、オーバラップ部分が凹部54に収容され、包装積層材料1の横シール部分の全体に均一に超音波が伝達される。
横シールするときには、超音波ホーン40とアンビル50により、包装積層材料1を挟持する。超音波ホーン40から、シールする包装積層材料1に最適な周波数と振幅の超音波を供給し、包装積層材料1を横シールする。例えば、15~40KHzの周波数で、10~40μmの振幅の超音波を100~500msecの時間、超音波ホーン40から供給する。
(横シール装置のアンビル)
次に、図6乃至9を用いて包装充填装置の横シール装置10のアンビル50の詳細について説明する。図6(a)はアンビル50の正面図であり、図6(b)はアンビル50の平面図である。図7はアンビル50のA-A′線断面図であり、図8はアンビル50のB-B′線断面図である。
次に、図6乃至9を用いて包装充填装置の横シール装置10のアンビル50の詳細について説明する。図6(a)はアンビル50の正面図であり、図6(b)はアンビル50の平面図である。図7はアンビル50のA-A′線断面図であり、図8はアンビル50のB-B′線断面図である。
包装充填装置の横シール装置10のアンビル50には、図6に示すように、矩形形状の受け面52が形成されている。
受け治具であるアンビル50の受け面52において、包装積層材料1の縁部を挟持する領域の形状を部分的に変更している。図6に示すように、アンビル50の受け面52の中央から所定距離にある領域P、Qにおける形状を部分的に変更している。
アンビル50の断面形状を、図7及び図8に示す。図7は、アンビル50の受け面52の基本的な断面形状である。図8は、アンビル50の受け面52の領域P、Qにおける、変更した部分の断面形状である。
図7(a)、図8(a)は、アンビル50全体の断面図であり、図7(b)、図8(b)は、図7(a)、図8(a)の拡大した部分的断面図であり、図7(c)、図8(c)は、図7(b)、図8(b)の更に拡大した部分的断面図である。
アンビル50の受け面52には、切断刃60の切断刃通過穴56の左右両側に、包装積層材料1に直接的に接触する接触部52Aが設けられている。包装積層材料1を接触部52Aと超音波ホーン40により挟持し、超音波により、接触部52Aに接触した部分が横シールされる。
アンビル50の受け面52の基本的な断面形状は、図7に示すように、接触部52Aの切断刃通過穴56側と反対側の隣接する部分に、傾斜部52Bを経て平坦部52Cが設けられ、更に傾斜部52Dを経て平坦部52Eが設けられている。
これに対し、アンビル50の受け面52の領域P、Qにおける断面形状は、図8に示すように、接触部52Aの切断刃通過穴56側と反対側の隣接する部分に、傾斜部52Bを経て平坦部52Cが設けられ、更に傾斜部52Dを経て平坦部52Eが設けられている。領域P、Qでは、基本的な断面形状と比較して、平坦部52Cの幅が狭く、傾斜部52Dの幅が広く傾斜が緩やかになっている。図8では、比較のため、基本的な断面形状を破線で示す。
アンビル50の受け面52の形状の詳細を図9に示す。図9はアンビル50の更に拡大した部分的断面図である。
図9(a)は図7に対応し、アンビル50の受け面52の基本的な断面形状である。
図9(a)において、アンビル50の受け面52の接触部52Aの幅は、例えば、1.0mmである。平坦部52Cは、接触部52Aの面と平行であり、接触部52Aより、例えば、0.10mm低くなっている、平坦部52Cの幅は、例えば、1.0mmである。傾斜部52Bは、接触面52Aと平坦部52Cとの間に位置している。傾斜部52Bの傾斜角度は、例えば、30度であり、傾斜部52Bの幅は、例えば、0.10mmである。平坦部52Eは、接触部52A及び平坦部52Cの面と平行であり、平坦部52Cより、例えば、0.10mm低くなっている、傾斜部52Dは、平坦部52Cと平坦部52Eの間に位置している。傾斜部52Dの傾斜角度は、例えば、30度である。傾斜部52Dの幅は、例えば、0.10mmである。
図9(b)は図8に対応し、アンビル50の受け面52の領域P、Qにおける断面形状である。図9(b)においては基本的な断面形状を破線で示している。
図9(b)において、アンビル50の受け面52の接触部52Aの幅は、例えば、0.5~3.0mmである。平坦部52Cは、接触部52Aの面と平行であり、接触部52Aより、例えば、0.05~0.20mm低くなっている、平坦部52Cの幅は、基本的な断面形状より短く、例えば、0.5~1.5mmである。傾斜部52Bは、接触面52Aと平坦部52Cとの間に位置している。傾斜部52Bの傾斜角度は、基本的な断面形状より小さく緩やかであり、例えば、15~25度であり、傾斜部52Bの幅は、例えば、0.05~0.20mmである。平坦部52Eは、接触部52A及び平坦部52Cの面と平行であり、平坦部52Cより、例えば、0.05~0.20mm低くなっている。傾斜部52Dは、平坦部52Cと平坦部52Eの間に位置している。傾斜部52Dの傾斜角度は、基本的な断面形状より緩やかであり、例えば、15~25度である。傾斜部52Dの幅は、例えば、0.10~0.20mmである。
図9(a)と図9(b)を比較すると明らかなように、アンビル50の受け面52の領域P、Qでは、他の領域とは異なり、傾斜部52Dの傾斜角度が緩やかになっている。
アンビル50の受け面52の領域P、Qでは包装積層材料1の縁部を挟持する。従来、包装積層材料1の縁部では、包装積層材料1が折り曲げられて挟持されているため、横シール時に塊状のポリエチレンが発生しやすい。塊状のポリエチレンが発生すると、ピンホールにより微小欠陥が発生する。
本実施形態では、アンビル50の受け面52の領域P、Qでの傾斜部52Dの傾斜角度が緩やかにすることにより、横シール時に塊状のポリエチレンが発生することを防止している。これによりピンホールにより微小欠陥の発生を防止している。
本願発明者等の鋭意研究によれば、アンビル50の受け面52の接触部52Aの隣接する部分に角張った部分がある場合に、包装積層材料1の縁部で横シール時に塊状のポリエチレンが発生しやすいことがわかった。
本実施形態では、平坦部52Cの幅を基本的な断面形状より短くし、傾斜部52Dの傾斜角度を基本的な断面形状より緩やかにすることにより、アンビル50の受け面52の接触部52Aの隣接する領域に角張った部分がないようにして、包装積層材料1の縁部で横シール時に塊状のポリエチレンの発生を防止している。
アンビル50の受け面52の接触部52Aの隣接する部分の形状としては、角張った部分がないようにするものであれば、図9(b)の形状に限らない。
例えば、図9(c)に示すように、平坦部52Cを設けることなく、接触面52Aから傾斜部52B、52Dを経て、平坦部52Eとなるようにしてもよい。図9(c)においては基本的な断面形状を破線で示している。平坦部52Cがないので、傾斜部52Dは、傾斜部52Bと平坦部52Eの間に位置している。傾斜部52Dの傾斜角度は、基本的な断面形状より更に緩やかであり、例えば、10~20度である。傾斜部52Dの幅は、例えば、1.0~3.0mmである。
また、図9(d)に示すような断面形状としてもよい。図9(d)においては基本的な断面形状を破線で示している。全体の断面形状は、基本的な断面形状と同様に、接触部52Aの切断刃通過穴56側と反対側の隣接する部分に、傾斜部52B、平坦部52C、傾斜部52D、平坦部52Eが設けられているが、接触部52Aと傾斜部52Bとの間の角部分と、平坦部52Cと傾斜部52Dとの間の角部分とを丸めている。接触部52Aと傾斜部52Bとの間の角部分を、例えば、直径5.0~10.0mmのR面取りし、平坦部52Cと傾斜部52Dとの間の角部分、例えば、直径5.0~10.0mmのR面取りしている。
このように本実施形態によれば、超音波シールによる包装積層材料の横シール時に塊状のポリエチレンが発生せず、良好な横シールを実現することができる。
[変形実施形態]
本発明は上記実施形態に限らず種々の変形が可能である。
本発明は上記実施形態に限らず種々の変形が可能である。
例えば、上記実施形態では、アンビルの一部の領域である領域P、Qにおいて、アンビルの断面形状を相違するようにしたが、これに限らない。アンビルの領域P、Q以外の領域においてアンビルの断面形状を相違するようにしてもよい。また、アンビルのすべての領域について、アンビルの断面形状を領域P、Qのような断面形状にしてもよい。
また、上記実施形態では、横シールに本発明を適用したが、縦シール等の他の個所のシールに本発明を適用してもよい。
1…包装積層材料
2…ストリップ
3…ストリップ付着装置
7…充填パイプ
8…縦シール装置
10…横シール装置
13…予備成形容器
14…包装容器
15…最終成形搬送装置
16…無菌室
30…アッパーチャンバ
33…エアナイフ
37…フォーミングリング
40…超音波ホーン
42…超音波供給面
44…ピエゾ素子
46…エアー室46
50…アンビル
52…受け面
52A…接触部
52B…傾斜部
52C…平坦部
52D…傾斜部
52E…平坦部
54…凹部
56…切断刃通過穴
60…切断刃
2…ストリップ
3…ストリップ付着装置
7…充填パイプ
8…縦シール装置
10…横シール装置
13…予備成形容器
14…包装容器
15…最終成形搬送装置
16…無菌室
30…アッパーチャンバ
33…エアナイフ
37…フォーミングリング
40…超音波ホーン
42…超音波供給面
44…ピエゾ素子
46…エアー室46
50…アンビル
52…受け面
52A…接触部
52B…傾斜部
52C…平坦部
52D…傾斜部
52E…平坦部
54…凹部
56…切断刃通過穴
60…切断刃
Claims (6)
- 帯状の包装材料に流動性食品を充填し、流動性食品を収容する包装容器を形成する包装充填装置であって、
超音波を供給する超音波供給部と、受け治具であるアンビルとを有し、前記超音波供給部の超音波供給面と前記アンビルの受け面とで前記帯状の包装材料を挟持し、挟持された前記帯状の包装材料に超音波を印加して、前記帯状の包装材料をシールするシール装置を有し、
前記アンビルの前記受け面が、シール時に前記帯状の包装材料と接触する接触部に隣接する領域における角部が滑らかである滑らか形状である
ことを特徴とする包装充填装置。 - 請求項1記載の包装充填装置において、
前記滑らか形状は、前記角部の頂角が155~175度の範囲内である滑らか形状である
ことを特徴とする包装充填装置。 - 請求項1又は2記載の包装充填装置において、
前記滑らか形状は、前記角部が面取りされている
ことを特徴とする包装充填装置。 - 請求項1乃至3のいずれか1項に記載の包装充填装置において、
前記アンビルの前記受け面の一部である所定領域が前記滑らか形状である
ことを特徴とする包装充填装置。 - 請求項4記載の包装充填装置において、
前記所定領域は、前記アンビルの前記受け面の中央からそれぞれ所定距離離れ、前記帯状の包装材料の縁部を挟持する2つの領域である
ことを特徴とする包装充填装置。 - 請求項1乃至5のいずれか1項に記載の包装充填装置において、
前記シール装置は、前記帯状の包装材料の長手方向に直交する方向で、前記帯状の包装材料をシールする
ことを特徴とする包装充填装置。
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201680011257.4A CN107249988B (zh) | 2015-02-20 | 2016-02-10 | 包装填充装置 |
| EP16752372.9A EP3260383A4 (en) | 2015-02-20 | 2016-02-10 | Packing/filling apparatus |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2015-031462 | 2015-02-20 | ||
| JP2015031462A JP6553890B2 (ja) | 2015-02-20 | 2015-02-20 | 包装充填装置 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2016132986A1 true WO2016132986A1 (ja) | 2016-08-25 |
Family
ID=56689242
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2016/053934 Ceased WO2016132986A1 (ja) | 2015-02-20 | 2016-02-10 | 包装充填装置 |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP3260383A4 (ja) |
| JP (1) | JP6553890B2 (ja) |
| CN (1) | CN107249988B (ja) |
| WO (1) | WO2016132986A1 (ja) |
Cited By (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN107640370A (zh) * | 2017-08-03 | 2018-01-30 | 上海普丽盛包装股份有限公司 | 一种液体灌装设备包装容器超声波密封装置 |
| EP3437841A1 (en) * | 2017-08-04 | 2019-02-06 | Tetra Laval Holdings & Finance S.A. | Anvil for transversally sealing a tube of packaging material and sealing jaw having an anvil |
| DE102017119273A1 (de) * | 2017-08-23 | 2019-02-28 | Herrmann Ultraschalltechnik Gmbh & Co. Kg | Schweißwerkzeug mit Siegelfläche |
| US10899082B2 (en) | 2017-07-17 | 2021-01-26 | Tetra Laval Holdings & Finance S.A. | Inductor coil for induction welding of a packaging material |
| US10994495B2 (en) | 2015-11-27 | 2021-05-04 | Tetra Laval Holdings & Finance S.A. | Sealing device with increased robustness |
| US11370571B2 (en) | 2017-07-18 | 2022-06-28 | Tetra Laval Holdings & Finance S.A. | Induction sealing device |
| US11534985B2 (en) | 2016-05-02 | 2022-12-27 | Tetra Laval Holdings & Finance S.A. | Induction sealing system |
| US11548238B2 (en) | 2018-09-10 | 2023-01-10 | Tetra Laval Holdings & Finance S.A. | Method for forming a tube and a method and a packaging machine for forming a package |
| US11554555B2 (en) | 2017-05-30 | 2023-01-17 | Tetra Laval Holdings & Finance S.A. | Apparatus for sealing the top of a package for a food product and system for forming and filling a food package |
| US11820540B2 (en) | 2018-09-11 | 2023-11-21 | Tetra Laval Holdings & Finance S.A. | Packaging apparatus for forming sealed packages |
| US12122547B2 (en) | 2019-02-05 | 2024-10-22 | Tetra Laval Holdings & Finance S.A. | Induction heat sealing device and a method for transversally seal a tube of packaging material |
| US12522394B2 (en) | 2021-02-15 | 2026-01-13 | Tetra Laval Holdings & Finance S.A. | Method for assessing quality of a transversal sealing of a food package |
Families Citing this family (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| SG11202103995XA (en) * | 2018-11-06 | 2021-05-28 | Nippon Paper Industries Co Ltd | Filling packaging machine, content filling container, and manufacturing method therefor |
| JP2023533291A (ja) * | 2020-07-08 | 2023-08-02 | テトラ ラバル ホールディングス アンド ファイナンス エス エイ | 横方向シールのためのインダクタ、横方向シールのためのインダクタを備える包装機、及びその方法 |
| CN116723927A (zh) * | 2021-04-07 | 2023-09-08 | 利乐拉瓦尔集团及财务有限公司 | 用于包装机的密封装置、具有密封装置的包装机以及操作密封装置的方法 |
| DE102021126679A1 (de) * | 2021-10-14 | 2023-04-20 | Herrmann Ultraschalltechnik Gmbh & Co. Kg | Werkzeug für eine Ultraschallschweißvorrichtung |
| US20240425216A1 (en) | 2021-11-19 | 2024-12-26 | Tetra Laval Holdings & Finance S.A. | Sealing device for a packaging machine, packaging machine having a sealing device and method of operating a sealing device |
| EP4461513B1 (en) * | 2023-05-12 | 2026-07-01 | Tetra Laval Holdings & Finance S.A. | ULTRASONIC SEALING SYSTEM AND ASSOCIATED ANVIL |
| JP2026515762A (ja) * | 2023-05-12 | 2026-05-19 | テトラ ラバル ホールディングス アンド ファイナンス エス エイ | 超音波シールシステム及びアンビル |
| CN121001870A (zh) * | 2023-05-12 | 2025-11-21 | 利乐拉瓦尔集团及财务有限公司 | 超声波密封系统及其砧座 |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2002326610A (ja) * | 2001-03-12 | 2002-11-12 | Tetra Laval Holdings & Finance Sa | 流動食品を充填された包装材料の壁部をシールする超音波横断シール方法および装置 |
| WO2006041377A1 (en) * | 2004-10-15 | 2006-04-20 | Tetra Laval Holdings & Finance S.A. | A method and an apparatus in ultrasonic sealing |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DK1241099T3 (da) * | 2001-03-12 | 2004-05-03 | Tetra Laval Holdings & Finance | Ultrasonisk forseglingsindretning til forsegling af emballager af hældbare fødevarer |
| DK1241098T3 (da) * | 2001-03-12 | 2004-05-24 | Tetra Laval Holdings & Finance | Ultrasonisk tværforseglingsindretning og ultrasonisk tværforseglingsfremgangsmåde til forsegling af vægge af et emballeringsmateriale fyldt med en hældbar fødevare |
| NL1037376C2 (nl) * | 2009-10-07 | 2011-04-11 | Robert Bosch Verpakkingsmachines B V | Inrichting voor het ultrasoon lassen van ten minste twee kunststoffen folielagen. |
| EP2368694A1 (en) * | 2010-03-22 | 2011-09-28 | Tetra Laval Holdings & Finance S.A. | Sonotrode |
| EP2774746B1 (en) * | 2013-03-07 | 2017-04-19 | Tetra Laval Holdings & Finance S.A. | Sonotrode |
-
2015
- 2015-02-20 JP JP2015031462A patent/JP6553890B2/ja active Active
-
2016
- 2016-02-10 WO PCT/JP2016/053934 patent/WO2016132986A1/ja not_active Ceased
- 2016-02-10 CN CN201680011257.4A patent/CN107249988B/zh active Active
- 2016-02-10 EP EP16752372.9A patent/EP3260383A4/en not_active Withdrawn
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2002326610A (ja) * | 2001-03-12 | 2002-11-12 | Tetra Laval Holdings & Finance Sa | 流動食品を充填された包装材料の壁部をシールする超音波横断シール方法および装置 |
| WO2006041377A1 (en) * | 2004-10-15 | 2006-04-20 | Tetra Laval Holdings & Finance S.A. | A method and an apparatus in ultrasonic sealing |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP3260383A4 * |
Cited By (21)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US10994495B2 (en) | 2015-11-27 | 2021-05-04 | Tetra Laval Holdings & Finance S.A. | Sealing device with increased robustness |
| US11534985B2 (en) | 2016-05-02 | 2022-12-27 | Tetra Laval Holdings & Finance S.A. | Induction sealing system |
| US11554555B2 (en) | 2017-05-30 | 2023-01-17 | Tetra Laval Holdings & Finance S.A. | Apparatus for sealing the top of a package for a food product and system for forming and filling a food package |
| US10899082B2 (en) | 2017-07-17 | 2021-01-26 | Tetra Laval Holdings & Finance S.A. | Inductor coil for induction welding of a packaging material |
| US11370571B2 (en) | 2017-07-18 | 2022-06-28 | Tetra Laval Holdings & Finance S.A. | Induction sealing device |
| CN107640370A (zh) * | 2017-08-03 | 2018-01-30 | 上海普丽盛包装股份有限公司 | 一种液体灌装设备包装容器超声波密封装置 |
| RU2726545C1 (ru) * | 2017-08-04 | 2020-07-14 | Тетра Лаваль Холдингз Энд Файнэнс С.А. | Опора для поперечного запечатывания трубы из упаковочного материала и сварочные зажимные губки с опорой |
| WO2019025367A1 (en) * | 2017-08-04 | 2019-02-07 | Tetra Laval Holdings & Finance S.A. | ENCLUME FOR SEALING TRANSVERSELY A PACKAGING MATERIAL TUBE AND SEALING JAW WITH AN ENCLOSURE |
| US10773846B2 (en) | 2017-08-04 | 2020-09-15 | Tetra Laval Holdings & Finance S.A. | Anvil for transversally sealing a tube of packaging material and sealing jaw having an anvil |
| EP3437841A1 (en) * | 2017-08-04 | 2019-02-06 | Tetra Laval Holdings & Finance S.A. | Anvil for transversally sealing a tube of packaging material and sealing jaw having an anvil |
| CN109383862B (zh) * | 2017-08-04 | 2021-07-13 | 利乐拉瓦尔集团及财务有限公司 | 用于横向密封包装材料管的砧座和具有砧座的密封钳 |
| CN109383862A (zh) * | 2017-08-04 | 2019-02-26 | 利乐拉瓦尔集团及财务有限公司 | 用于横向密封包装材料管的砧座和具有砧座的密封钳 |
| JP7191931B2 (ja) | 2017-08-04 | 2022-12-19 | テトラ ラバル ホールディングス アンド ファイナンス エス エイ | 包装材料のチューブを横方向に密封するためのアンビル、及びアンビルを有する密封用ジョー |
| JP2020529370A (ja) * | 2017-08-04 | 2020-10-08 | テトラ ラバル ホールディングス アンド ファイナンス エス エイ | 包装材料のチューブを横方向に密封するためのアンビル、及びアンビルを有する密封用ジョー |
| DE102017119273A1 (de) * | 2017-08-23 | 2019-02-28 | Herrmann Ultraschalltechnik Gmbh & Co. Kg | Schweißwerkzeug mit Siegelfläche |
| US11820082B2 (en) | 2017-08-23 | 2023-11-21 | Herrmann Ultraschalltechnik Gmbh & Co. Kg | Welding method for a multilayer composite having a barrier layer |
| US11548238B2 (en) | 2018-09-10 | 2023-01-10 | Tetra Laval Holdings & Finance S.A. | Method for forming a tube and a method and a packaging machine for forming a package |
| US11820540B2 (en) | 2018-09-11 | 2023-11-21 | Tetra Laval Holdings & Finance S.A. | Packaging apparatus for forming sealed packages |
| US12122547B2 (en) | 2019-02-05 | 2024-10-22 | Tetra Laval Holdings & Finance S.A. | Induction heat sealing device and a method for transversally seal a tube of packaging material |
| US12240643B2 (en) | 2019-02-05 | 2025-03-04 | Tetra Laval Holdings & Finance S.A. | Induction heat sealing device and a method for transversally seal a tube of packaging material |
| US12522394B2 (en) | 2021-02-15 | 2026-01-13 | Tetra Laval Holdings & Finance S.A. | Method for assessing quality of a transversal sealing of a food package |
Also Published As
| Publication number | Publication date |
|---|---|
| JP2016153317A (ja) | 2016-08-25 |
| EP3260383A1 (en) | 2017-12-27 |
| JP6553890B2 (ja) | 2019-07-31 |
| EP3260383A4 (en) | 2018-10-31 |
| CN107249988B (zh) | 2020-02-07 |
| CN107249988A (zh) | 2017-10-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6553890B2 (ja) | 包装充填装置 | |
| RU2726545C1 (ru) | Опора для поперечного запечатывания трубы из упаковочного материала и сварочные зажимные губки с опорой | |
| US10807751B2 (en) | Anvil and ultrasonic sealing apparatus | |
| JP6071879B2 (ja) | 密封包装体の製造方法及び製造装置 | |
| JP5778243B2 (ja) | ソノトロード | |
| JP6461827B2 (ja) | ソノトロード | |
| CN109070487B (zh) | 改进的感应密封系统 | |
| MX2010011364A (es) | Mordaza selladora para producir empaques sellados de un producto alimenticio. | |
| KR101872656B1 (ko) | 포장용 필름으로의 박리 용이 부분 형성방법, 박리 용이 부분을 갖는 포장봉지 및 충전 포장기 | |
| RU2757009C2 (ru) | Питьевая соломинка и способ изготовления питьевой соломинки | |
| JP2019508339A (ja) | 密封パックからパッケージを製造するための折り畳みユニットおよび密封パックからパッケージを製造するための方法 | |
| JP2002337821A (ja) | 流動食品のパッケージをシールする超音波シール装置 | |
| US10343800B2 (en) | Ultrasonic sealing apparatus | |
| CN109070484A (zh) | 生产密封包装单元的组件 | |
| JP2019513652A (ja) | ソノトロード | |
| JP2015024839A (ja) | 包装充填装置 | |
| WO2020105664A1 (ja) | 接着方法および接着装置 | |
| JP2008143523A (ja) | 包装充填装置 | |
| BR112020001482B1 (pt) | Bigorna, e, garra de vedação. | |
| HK1032939B (en) | Ultrasonic sealing apparatus | |
| HK1032939A1 (en) | Ultrasonic sealing apparatus |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 16752372 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| REEP | Request for entry into the european phase |
Ref document number: 2016752372 Country of ref document: EP |