WO2018193811A1 - タイヤ - Google Patents
タイヤ Download PDFInfo
- Publication number
- WO2018193811A1 WO2018193811A1 PCT/JP2018/013439 JP2018013439W WO2018193811A1 WO 2018193811 A1 WO2018193811 A1 WO 2018193811A1 JP 2018013439 W JP2018013439 W JP 2018013439W WO 2018193811 A1 WO2018193811 A1 WO 2018193811A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- tire
- thermoplastic elastomer
- resin material
- copolymer
- polyester
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B60—VEHICLES IN GENERAL
- B60C—VEHICLE TYRES; TYRE INFLATION; TYRE CHANGING; CONNECTING VALVES TO INFLATABLE ELASTIC BODIES IN GENERAL; DEVICES OR ARRANGEMENTS RELATED TO TYRES
- B60C1/00—Tyres characterised by the chemical composition or the physical arrangement or mixture of the composition
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B60—VEHICLES IN GENERAL
- B60C—VEHICLE TYRES; TYRE INFLATION; TYRE CHANGING; CONNECTING VALVES TO INFLATABLE ELASTIC BODIES IN GENERAL; DEVICES OR ARRANGEMENTS RELATED TO TYRES
- B60C1/00—Tyres characterised by the chemical composition or the physical arrangement or mixture of the composition
- B60C1/0016—Compositions of the tread
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B60—VEHICLES IN GENERAL
- B60C—VEHICLE TYRES; TYRE INFLATION; TYRE CHANGING; CONNECTING VALVES TO INFLATABLE ELASTIC BODIES IN GENERAL; DEVICES OR ARRANGEMENTS RELATED TO TYRES
- B60C1/00—Tyres characterised by the chemical composition or the physical arrangement or mixture of the composition
- B60C1/0025—Compositions of the sidewalls
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B60—VEHICLES IN GENERAL
- B60C—VEHICLE TYRES; TYRE INFLATION; TYRE CHANGING; CONNECTING VALVES TO INFLATABLE ELASTIC BODIES IN GENERAL; DEVICES OR ARRANGEMENTS RELATED TO TYRES
- B60C5/00—Inflatable pneumatic tyres or inner tubes
- B60C5/01—Inflatable pneumatic tyres or inner tubes without substantial cord reinforcement, e.g. cordless tyres, cast tyres
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L67/00—Compositions of polyesters obtained by reactions forming a carboxylic ester link in the main chain; Compositions of derivatives of such polymers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B60—VEHICLES IN GENERAL
- B60C—VEHICLE TYRES; TYRE INFLATION; TYRE CHANGING; CONNECTING VALVES TO INFLATABLE ELASTIC BODIES IN GENERAL; DEVICES OR ARRANGEMENTS RELATED TO TYRES
- B60C9/00—Reinforcements or ply arrangement of pneumatic tyres
- B60C9/02—Carcasses
- B60C2009/0269—Physical properties or dimensions of the carcass coating rubber
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B60—VEHICLES IN GENERAL
- B60C—VEHICLE TYRES; TYRE INFLATION; TYRE CHANGING; CONNECTING VALVES TO INFLATABLE ELASTIC BODIES IN GENERAL; DEVICES OR ARRANGEMENTS RELATED TO TYRES
- B60C11/00—Tyre tread bands; Tread patterns; Anti-skid inserts
- B60C11/0008—Tyre tread bands; Tread patterns; Anti-skid inserts characterised by the tread rubber
- B60C2011/0016—Physical properties or dimensions
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B60—VEHICLES IN GENERAL
- B60C—VEHICLE TYRES; TYRE INFLATION; TYRE CHANGING; CONNECTING VALVES TO INFLATABLE ELASTIC BODIES IN GENERAL; DEVICES OR ARRANGEMENTS RELATED TO TYRES
- B60C13/00—Tyre sidewalls; Protecting, decorating, marking, or the like, thereof
- B60C2013/005—Physical properties of the sidewall rubber
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L2207/00—Properties characterising the ingredient of the composition
- C08L2207/04—Thermoplastic elastomer
Definitions
- This disclosure relates to tires.
- thermoplastic resins particularly thermoplastic resins and thermoplastic elastomers, as materials
- thermoplastic polymer materials that is, thermoplastic resins
- a tire that is formed of a thermoplastic resin material and has an annular tire skeleton, and has a reinforcing cord member that is wound in the circumferential direction around the outer periphery of the tire skeleton to form a reinforcing cord layer
- a plastic resin material contains at least a polyester-based thermoplastic elastomer
- the state of the resin material in the tire after manufacture affects the state of the tire skeleton. Therefore, if the state of the resin material can be appropriately controlled, it is considered that the characteristics (for example, durability, etc.) of the tire frame body and the tire can be improved to a desired state. However, there is still room for study as to how the state of the resin material is controlled to achieve the desired characteristics.
- an object of the present disclosure is to provide a tire having a tire skeleton body including a thermoplastic elastomer as a resin contained in a resin material and having excellent durability.
- thermoplastic resin is a concept including a thermoplastic resin, a thermoplastic elastomer, and a thermosetting resin, and does not include vulcanized rubber.
- “same species” means those having a skeleton that is common to the skeleton constituting the main chain of the resin, such as esters and styrenes.
- thermoplastic elastomer refers to a polymer that forms a crystalline hard segment with a high melting point, or a hard segment with a high cohesive force, and a polymer that forms an amorphous soft segment with a low glass transition temperature. The polymer compound which consists of a copolymer which has these.
- thermoplastic elastomer is softened and fluidized as the temperature rises, and becomes relatively hard and strong when cooled.
- the thermoplastic elastomer is a polymer compound having rubber-like elasticity.
- hard segment refers to a component that is relatively harder than the soft segment
- soft segment refers to a component that is relatively softer than the hard segment.
- the hard segment is preferably a molecular constraint component that serves as a crosslinking point of the crosslinked rubber that prevents plastic deformation.
- the soft segment is preferably a flexible component exhibiting rubber elasticity.
- a numerical range expressed using “to” means a range including numerical values described before and after “to” as a lower limit value and an upper limit value.
- the term “process” includes not only an independent process but also a process that can be clearly distinguished from other processes as long as the purpose is achieved. include.
- the tire according to the present embodiment has a tire skeleton formed of a resin material containing a thermoplastic elastomer (that is, part or all of which is formed only of the resin material).
- the thickness La of the amorphous portion measured by the small-angle X-ray scattering method of the thermoplastic elastomer is in the range of 12.3 nm to 13.9 nm.
- a tire having a tire skeleton formed using a thermoplastic elastomer having a non-crystalline portion thickness La in the above range is a thermoplastic having a non-crystalline portion thickness La in the above range. It has been clarified that the tire has a durability (particularly, crack resistance) as compared with a tire having a tire skeleton formed using only an elastomer.
- the thickness La of the amorphous part of the thermoplastic elastomer is the thickness of one amorphous part in the repeating structure of the crystal part and the amorphous part of the hard segment of the thermoplastic elastomer.
- the thickness La of the amorphous part is measured by a small-angle X-ray scattering method as described below using a sample collected from the tire frame or a sample prepared from a resin material used for forming the tire frame. Is done.
- the long period L is defined as 2 ⁇ / q max .
- q max is the wave number q [nm ⁇ 1 ] where the primary peak of small-angle X-ray scattering is shown.
- a tire having a tire skeleton formed using a thermoplastic elastomer having an amorphous part thickness La in the above range is excellent in durability.
- the reason is not clear, but is presumed as follows.
- a thickness La of the amorphous part of 12.3 nm or more is considered to indicate that the molecular chain of the amorphous part is extended in the repeating structure of the crystal part and the amorphous part of the hard segment.
- the orientation of the molecular chain in the amorphous part that is, the degree of alignment
- it is considered that the cushioning property of the thermoplastic elastomer is enhanced, and the durability of the tire, particularly the crack resistance against impact, is improved.
- the thickness La of the amorphous part is 13.9 nm or less, it indicates that the molecular chain of the amorphous part is not excessively extended in the repeating structure of the crystalline part and the amorphous part of the hard segment. Conceivable. Therefore, a decrease in the strength of the molecular chain in the amorphous part due to excessive elongation is suppressed. Thereby, it is considered that the strength of the thermoplastic elastomer is ensured and the durability of the tire, particularly the crack resistance against impact, is improved.
- the thickness La of the amorphous part is further preferably in the range of 12.5 nm to 13.7 nm, and more preferably in the range of 12.8 nm to 13.4 nm.
- the method for controlling the value of the thickness La of the amorphous part of the thermoplastic elastomer is not particularly limited.
- the value of the thickness La of the amorphous portion can be reduced by increasing the heating temperature at the time of forming the tire frame (for example, the cylinder temperature or mold temperature at the time of injection molding).
- the value of the thickness La of the amorphous part can be increased by lowering the heating temperature (for example, the cylinder temperature or the mold temperature) at the time of forming the tire skeleton.
- the long period L measured by the small-angle X-ray scattering method of the thermoplastic elastomer contained in the tire skeleton is in the range of 15.6 nm to 17.1 nm.
- the long period L of the thermoplastic elastomer is the repetitive structure of the crystal part and the amorphous part of the hard segment in the thermoplastic elastomer, and the crystal part in the repeating unit composed of one crystal part and one amorphous part. It is the total value of the thickness and the thickness of the amorphous part.
- the long period L is calculated as follows by a small angle X-ray scattering method using a sample collected from a tire frame or a sample prepared from a resin material used for forming the tire frame.
- the one-dimensional autocorrelation function ⁇ (r) obtained from the value of the one-dimensional autocorrelation function is plotted against r, and the value of r taking the primary peak is taken.
- Q in the formula represents the wave number [nm ⁇ 1 ] where the primary peak of the small-angle X-ray scattering is shown.
- R has a dimension of distance at any point in the polymer space.
- I (q) represents the X-ray scattering intensity.
- One-dimensional autocorrelation function ⁇ (r) ( ⁇ I (q) q 2 cos (rq) dq) / ( ⁇ I (q) q 2 dq)
- the durability of the tire is improved. This is thought to be because the long period L is 15.6 nm or more, which reduces the friction between molecules and improves the durability of the tire. Further, when the thickness is 17.1 nm or less, an increase in elastic modulus due to excessive elongation of the molecular chain is suppressed, and it is considered that the durability of the tire is also improved from this viewpoint.
- the long period L is further preferably in the range of 15.8 nm to 17.0 nm, and more preferably in the range of 16.1 nm to 16.7 nm.
- the value of the long period L increases as the thickness La of the amorphous part in the thermoplastic elastomer increases. Moreover, the growth of the crystal part in the thermoplastic elastomer is promoted, and the crystal part becomes thicker as the thickness of the crystal part increases. In addition, it exists in the tendency for melting
- the method for controlling the value of the long period L of the thermoplastic elastomer is not particularly limited.
- a method of controlling the value of the thickness La of the amorphous part can be mentioned.
- the long period L can be increased by increasing the heating temperature (for example, cylinder temperature or mold temperature) at the time of forming the tire skeleton and increasing the time required for cooling to promote crystal growth.
- the long period L can be reduced by lowering the heating temperature (for example, the cylinder temperature and the mold temperature) at the time of forming the tire skeleton to shorten the time required for cooling and suppressing the crystal growth.
- the degree of orientation f of the thermoplastic elastomer contained in the tire skeleton measured by the small angle X-ray scattering method is in the range of ⁇ 0.08 to 0.08 (that is, the degree of orientation f is The absolute value is preferably 0 or more and 0.08 or less).
- the orientation degree f of the thermoplastic elastomer means the orientation degree of molecules in the crystal part of the hard segment in the thermoplastic elastomer.
- orientation degree f is in the range of -0.08 to 0.08, the durability of the tire, particularly the crack resistance against impact, is improved. This is presumed to be because, when the degree of orientation f is within the above range, the mechanical input to the tire frame during traveling can be effectively dispersed, and the mechanical strength is increased.
- the orientation degree f is further preferably in the range of -0.08 to 0.04, and more preferably in the range of -0.02 to 0.02.
- the method for controlling the value of the orientation degree f of the thermoplastic elastomer is not particularly limited. For example, it can be carried out by changing the temperature of the thermoplastic elastomer, the cylinder temperature, the mold temperature, the cooling rate, etc. at the time of injection molding when forming the tire skeleton. For example, increasing the temperature at the time of injection molding of a thermoplastic elastomer (that is, increasing the temperature of the thermoplastic elastomer) decreases the viscosity, increases the cylinder temperature or mold temperature, and increases the time required for cooling, thereby increasing the molecular weight.
- the degree of orientation f can be reduced by relaxing the movement.
- the degree of crystallinity Xc of the thermoplastic elastomer contained in the tire skeleton measured by the wide angle X-ray scattering method is in the range of 12% to 45%.
- the crystallinity Xc of the thermoplastic elastomer represents the ratio of the crystal part in the hard segment of the thermoplastic elastomer. Note that the larger the value of the crystallinity Xc, the larger the proportion of crystal parts and the smaller the proportion of amorphous parts.
- the crystallinity Xc is in the range of 12% to 45%, the durability of the tire, particularly the crack resistance against impact, is improved. This is presumably because when the crystallinity Xc is 12% or more, the heat resistance is increased. Further, it is presumed that when the crystallinity degree Xc is 45% or less, the destruction phenomenon due to the crystal starting point is suppressed.
- the crystallinity Xc is more preferably 12% to 37%.
- the method for controlling the value of the crystallinity Xc of the thermoplastic elastomer is not particularly limited.
- the crystallinity Xc can be increased by increasing the heating temperature (for example, cylinder temperature or mold temperature) at the time of forming the tire skeleton and increasing the time required for cooling to promote crystal growth.
- the degree of crystallinity Xc can be reduced by lowering the mold temperature during cooling to shorten the time required for cooling and suppressing crystal growth.
- the resin material includes a thermoplastic elastomer, and may optionally include a component other than the thermoplastic elastomer such as an additive.
- the kind of thermoplastic elastomer used for formation of a tire frame is not particularly limited.
- polyester-based thermoplastic elastomer (TPC), polyamide-based thermoplastic elastomer (TPA), polystyrene-based thermoplastic elastomer (TPS), polyurethane-based thermoplastic elastomer (TPU), olefin-based thermoplastic elastomer (TPO), thermoplastic rubber A crosslinked body (TPV), other thermoplastic elastomers (TPZ), etc. are mentioned.
- JIS K6418 can be referred to.
- thermoplastic elastomer a polyester-based thermoplastic elastomer is preferable as the thermoplastic elastomer because of its advantage that the bending fatigue resistance is higher than that of other thermoplastic elastomers.
- a tire containing a polyester-based thermoplastic elastomer exhibits high durability by suppressing the occurrence and growth of fatigue cracks against repeated bending due to its high bending fatigue resistance.
- the polyester-based thermoplastic elastomer is a polymer compound having elasticity, a polymer containing a polyester that forms a crystalline hard segment with a high melting point, and a polymer that forms an amorphous soft segment with a low glass transition temperature, It is a thermoplastic resin material made of a copolymer having.
- the polyester-based thermoplastic elastomer means one having a partial structure made of polyester in the structure. Examples of the polyester-based thermoplastic elastomer include ester-based thermoplastic elastomer (TPC) defined in JIS K6418: 2007.
- polyester-based thermoplastic elastomer for example, at least a polyester is crystalline and a hard segment having a high melting point is formed, and another polymer (eg, polyester or polyether) is amorphous and has a low glass transition temperature.
- another polymer eg, polyester or polyether
- polyester forming the hard segment for example, aromatic polyester can be used.
- the aromatic polyester can be formed from, for example, an aromatic dicarboxylic acid or an ester-forming derivative thereof and an aliphatic diol.
- aromatic polyester examples include polybutylene terephthalate derived from terephthalic acid and / or dimethyl terephthalate and 1,4-butanediol. Further, isophthalic acid, phthalic acid, naphthalene-2,6-dicarboxylic acid, naphthalene-2,7-dicarboxylic acid, diphenyl-4,4′-dicarboxylic acid, diphenoxyethanedicarboxylic acid, 5-sulfoisophthalic acid, or these A dicarboxylic acid component such as an ester-forming derivative, and a diol having a molecular weight of 300 or less (for example, an aliphatic diol such as ethylene glycol, trimethylene glycol, pentamethylene glycol, hexamethylene glycol, neopentyl glycol, and decamethylene glycol, 1 , 4-cyclohexanedimethanol, and cycloaliphatic diols such as tricycl
- polyester forming the hard segment examples include polyethylene terephthalate, polybutylene terephthalate, polymethylene terephthalate, polyethylene naphthalate, and polybutylene naphthalate. Of these, polybutylene terephthalate is preferable.
- Aliphatic polyethers include poly (ethylene oxide) glycol, poly (propylene oxide) glycol, poly (tetramethylene oxide) glycol, poly (hexamethylene oxide) glycol, copolymers of ethylene oxide and propylene oxide, poly (propylene oxide) And ethylene oxide addition polymer of glycol, and a copolymer of ethylene oxide and tetrahydrofuran.
- the aliphatic polyester include poly ( ⁇ -caprolactone), polyenantlactone, polycaprylolactone, polybutylene adipate, and polyethylene adipate.
- poly (tetramethylene oxide) glycol poly (propylene oxide) glycol are polymers that form soft segments from the viewpoint of the elastic properties of the resulting polyester block copolymer.
- Preferred are ethylene oxide adducts, poly ( ⁇ -caprolactone), polybutylene adipate, and polyethylene adipate.
- the number average molecular weight of the polymer forming the hard segment (that is, polyester) is preferably 300 to 6000 from the viewpoint of toughness and low temperature flexibility.
- the number average molecular weight of the polymer forming the soft segment is preferably 300 to 6000 from the viewpoint of toughness and low temperature flexibility.
- the mass ratio (x: y) between the hard segment (x) and the soft segment (y) is preferably 99: 1 to 20:80, and 98: 2 to 30: from the viewpoint of moldability of the tire frame body. 70 is more preferable.
- the combination of the hard segment and the soft segment described above examples include, for example, combinations of the hard segment and the soft segment mentioned above.
- the combination of the hard segment and the soft segment described above is preferably a combination in which the hard segment is polybutylene terephthalate, the soft segment is an aliphatic polyether, and the hard segment is polybutylene terephthalate. More preferred is a combination wherein is poly (ethylene oxide) glycol.
- polyester-based thermoplastic elastomers examples include “Hytrel” series (for example, 3046, 5557, 6347, 4047N, and 4767N) manufactured by Toray DuPont Co., Ltd., and “Perprene” manufactured by Toyobo Co., Ltd. Series (for example, P30B, P40B, P40H, P55B, P70B, P150B, P280B, E450B, P150M, S1001, S2001, S5001, S6001, and S9001) can be used.
- Hytrel for example, 3046, 5557, 6347, 4047N, and 4767N
- Perprene manufactured by Toyobo Co., Ltd. Series
- the polyester-based thermoplastic elastomer can be synthesized by copolymerizing a polymer that forms a hard segment and a polymer that forms a soft segment by a known method.
- the content of the polyester thermoplastic elastomer in the total thermoplastic elastomer contained is not particularly limited, but the total amount of all resins Is preferably 50% by mass or more, more preferably 80% by mass or more, and still more preferably 90% by mass or more.
- the polyester-based thermoplastic elastomer can sufficiently exhibit the characteristics, and the durability of the tire is further improved. It becomes easy.
- the polyamide-based thermoplastic elastomer is a thermoplastic resin comprising a copolymer having a crystalline polymer having a high melting point and a non-crystalline polymer having a low glass transition temperature. It means a material having an amide bond (—CONH—) in the main chain of the polymer forming the hard segment.
- a soft segment in which at least polyamide is crystalline and a high melting point is formed and another polymer (for example, polyester or polyether) is amorphous and has a low glass transition temperature.
- the material which forms is mentioned.
- the polyamide-based thermoplastic elastomer may be formed using a chain extender such as dicarboxylic acid in addition to the hard segment and the soft segment.
- a chain extender such as dicarboxylic acid
- Specific examples of polyamide-based thermoplastic elastomers include amide-based thermoplastic elastomers (TPA) defined in JIS K6418: 2007, polyamide-based elastomers described in JP-A No. 2004-346273, and the like. it can.
- examples of the polyamide forming the hard segment include polyamides produced by monomers represented by the following general formula (1) or general formula (2).
- R 1 represents a molecular chain of a hydrocarbon having 2 to 20 carbon atoms (for example, an alkylene group having 2 to 20 carbon atoms).
- R 2 represents a hydrocarbon molecular chain having 3 to 20 carbon atoms (for example, an alkylene group having 3 to 20 carbon atoms).
- R 1 is preferably a hydrocarbon molecular chain having 3 to 18 carbon atoms (for example, an alkylene group having 3 to 18 carbon atoms), and a hydrocarbon molecular chain having 4 to 15 carbon atoms (for example, (Alkylene group having 4 to 15 carbon atoms) is more preferable, and a molecular chain of a hydrocarbon having 10 to 15 carbon atoms (for example, an alkylene group having 10 to 15 carbon atoms) is particularly preferable.
- R 2 is preferably a hydrocarbon molecular chain having 3 to 18 carbon atoms (eg, an alkylene group having 3 to 18 carbon atoms), and a hydrocarbon molecular chain having 4 to 15 carbon atoms.
- an alkylene group having 4 to 15 carbon atoms is more preferable, and a molecular chain of a hydrocarbon having 10 to 15 carbon atoms (for example, an alkylene group having 10 to 15 carbon atoms) is particularly preferable.
- the monomer represented by the general formula (1) or the general formula (2) include ⁇ -aminocarboxylic acid or lactam.
- the polyamide forming the hard segment include polycondensates of these ⁇ -aminocarboxylic acids or lactams, and copolycondensation polymers of diamines and dicarboxylic acids.
- Examples of ⁇ -aminocarboxylic acids include 6 to 20 carbon atoms such as 6-aminocaproic acid, 7-aminoheptanoic acid, 8-aminooctanoic acid, 10-aminocapric acid, 11-aminoundecanoic acid, and 12-aminododecanoic acid.
- Examples of the lactam include aliphatic lactams having 5 to 20 carbon atoms such as lauryl lactam, ⁇ -caprolactam, udecan lactam, ⁇ -enantolactam, and 2-pyrrolidone.
- diamine examples include ethylene diamine, trimethylene diamine, tetramethylene diamine, hexamethylene diamine, heptamethylene diamine, octamethylene diamine, nonamethylene diamine, decamethylene diamine, undecamethylene diamine, dodecamethylene diamine, 2, 2, 4
- diamine compounds such as aliphatic diamines having 2 to 20 carbon atoms such as trimethylhexamethylenediamine, 2,4,4-trimethylhexamethylenediamine, 3-methylpentamethylenediamine, and metaxylenediamine.
- the dicarboxylic acid can be represented by HOOC- (R 3 ) m —COOH (R 3 : a hydrocarbon molecular chain having 3 to 20 carbon atoms, m: 0 or 1).
- R 3 a hydrocarbon molecular chain having 3 to 20 carbon atoms, m: 0 or 1.
- oxalic acid, succinic acid And aliphatic dicarboxylic acids having 2 to 20 carbon atoms such as glutaric acid, adipic acid, pimelic acid, suberic acid, azelaic acid, sebacic acid, and dodecanedioic acid.
- a polyamide obtained by ring-opening polycondensation of lauryl lactam, ⁇ -caprolactam, or decane lactam can be preferably used.
- polyester, polyether, etc. are mentioned, for example.
- Specific examples include polyethylene glycol, polypropylene glycol, polytetramethylene ether glycol, and ABA type triblock polyether. These can be used alone or in combination of two or more.
- polyether diamine etc. which are obtained by making ammonia etc. react with the terminal of polyether can also be used.
- the “ABA type triblock polyether” means a polyether represented by the following general formula (3).
- x and z represent an integer of 1 to 20.
- y represents an integer of 4 to 50.
- each of x and z is preferably an integer of 1 to 18, more preferably an integer of 1 to 16, still more preferably an integer of 1 to 14, and particularly preferably an integer of 1 to 12.
- y is preferably an integer of 5 to 45, more preferably an integer of 6 to 40, still more preferably an integer of 7 to 35, and particularly preferably an integer of 8 to 30.
- combinations of the hard segment and the soft segment include a combination of a ring-opening polycondensate of lauryl lactam and polyethylene glycol, a combination of a ring-opening polycondensate of lauryl lactam and polypropylene glycol, and a ring opening of lauryl lactam.
- a combination of a polycondensate and a polytetramethylene ether glycol, or a ring-opening polycondensate of lauryl lactam and an ABA type triblock polyether is preferred, and a ring opening polycondensate of lauryl lactam and an ABA type triblock polyether The combination with is more preferable.
- the number average molecular weight of the polymer forming the hard segment is preferably 300 to 15000 from the viewpoint of melt moldability.
- the number average molecular weight of the polymer forming the soft segment is preferably 200 to 6000 from the viewpoint of toughness and low temperature flexibility.
- the mass ratio (x: y) of the hard segment (x) and the soft segment (y) is preferably 50:50 to 90:10, and preferably 50:50 to 80:20 from the viewpoint of moldability of the tire frame body. Is more preferable.
- the polyamide-based thermoplastic elastomer can be synthesized by copolymerizing a polymer forming a hard segment and a polymer forming a soft segment by a known method.
- Examples of commercially available products of polyamide-based thermoplastic elastomer include, for example, “UBESTA XPA” series (for example, XPA9063X1, XPA9055X1, XPA9048X2, XPA9048X1, XPA9040X1, XPA9040X2XPA9044, etc.) manufactured by Daicel Eponic Corporation. “Vestamide” series (for example, E40-S3, E47-S1, E47-S3, E55-S1, E55-S3, EX9200, E50-R2, etc.) can be used.
- polystyrene-based thermoplastic elastomer for example, at least polystyrene forms a hard segment, and other polymers (for example, polybutadiene, polyisoprene, polyethylene, hydrogenated polybutadiene, hydrogenated polyisoprene, etc.) Examples thereof include materials that form amorphous soft segment having a low glass transition temperature.
- polystyrene forming the hard segment for example, those obtained by a known radical polymerization method or ionic polymerization method are preferably used, and specifically, polystyrene having anion living polymerization can be mentioned.
- the polymer forming the soft segment include polybutadiene, polyisoprene, and poly (2,3-dimethyl-butadiene).
- the combination of the hard segment and the soft segment mentioned above can be mentioned.
- the combination of the hard segment and the soft segment is preferably a combination of polystyrene and polybutadiene or a combination of polystyrene and polyisoprene.
- the soft segment is preferably hydrogenated.
- the number average molecular weight of the polymer forming the hard segment is preferably from 5,000 to 500,000, more preferably from 10,000 to 200,000. Further, the number average molecular weight of the polymer forming the soft segment is preferably from 5,000 to 1,000,000, more preferably from 10,000 to 800,000, and even more preferably from 30,000 to 500,000. Further, the volume ratio (x: y) of the hard segment (x) and the soft segment (y) is preferably 5:95 to 80:20 from the viewpoint of moldability of the tire frame body, and 10:90 to 70:30. Is more preferable.
- the polystyrene-based thermoplastic elastomer can be synthesized by copolymerizing a polymer forming a hard segment and a polymer forming a soft segment by a known method.
- polystyrene-based thermoplastic elastomers include styrene-butadiene copolymers [for example, SBS (polystyrene-poly (butylene) block-polystyrene) and SEBS (polystyrene-poly (ethylene / butylene) block-polystyrene)], styrene.
- -Isoprene copolymer eg polystyrene-polyisoprene block-polystyrene
- styrene-propylene copolymer eg SEP (polystyrene- (ethylene / propylene) block), SEPS (polystyrene-poly (ethylene / propylene) block-polystyrene) ), SEEPS (polystyrene-poly (ethylene-ethylene / propylene) block-polystyrene), SEB (polystyrene (ethylene / butylene) block)] and the like.
- SEP polystyrene- (ethylene / propylene) block
- SEPS polystyrene-poly (ethylene / propylene) block-polystyrene
- SEEPS polystyrene-poly (ethylene-ethylene / propylene) block-polystyrene
- thermoplastic elastomer As a commercially available product of polystyrene-based thermoplastic elastomer, for example, “Tough Tech” series manufactured by Asahi Kasei Corporation (for example, H1031, H1041, H1043, H1051, H1052, H1053, H1062, H1082, H1141, H1221, and H1272 etc.) "SEBS” series (8007, 8076, etc.) and “SEPS” series (2002, 2063, etc.) manufactured by Kuraray Co., Ltd. can be used.
- “Tough Tech” series manufactured by Asahi Kasei Corporation for example, H1031, H1041, H1043, H1051, H1052, H1053, H1062, H1082, H1141, H1221, and H1272 etc.
- SEBS 8007, 8076, etc.
- SEPS 2002, 2063, etc.
- thermoplastic elastomer As polyurethane-based thermoplastic elastomers, for example, at least polyurethane forms a hard segment in which pseudo-crosslinking is formed by physical aggregation, and other polymers form a soft segment with a low glass transition temperature that is amorphous. Material.
- Specific examples of the polyurethane-based thermoplastic elastomer include a polyurethane-based thermoplastic elastomer (TPU) defined in JIS K6418: 2007.
- TPU polyurethane-based thermoplastic elastomer
- the polyurethane-based thermoplastic elastomer can be represented as a copolymer including a soft segment including a unit structure represented by the following formula A and a hard segment including a unit structure represented by the following formula B.
- P represents a long-chain aliphatic polyether or a long-chain aliphatic polyester.
- R represents an aliphatic hydrocarbon, an alicyclic hydrocarbon, or an aromatic hydrocarbon.
- P ′ represents a short chain aliphatic hydrocarbon, an alicyclic hydrocarbon, or an aromatic hydrocarbon.
- the long-chain aliphatic polyether or long-chain aliphatic polyester represented by P for example, those having a molecular weight of 500 to 5000 can be used.
- P is derived from a diol compound containing a long-chain aliphatic polyether represented by P or a long-chain aliphatic polyester.
- diol compounds include polyethylene glycol, polypropylene glycol, polytetramethylene ether glycol, poly (butylene abido) diol, poly- ⁇ -caprolactone diol, poly (hexamethylene carbonate) having a molecular weight within the above range.
- Diol, ABA type triblock polyether and the like These can be used alone or in combination of two or more.
- R is derived from a diisocyanate compound containing an aliphatic hydrocarbon, an alicyclic hydrocarbon, or an aromatic hydrocarbon represented by R.
- the aliphatic diisocyanate compound containing an aliphatic hydrocarbon represented by R include 1,2-ethylene diisocyanate, 1,3-propylene diisocyanate, 1,4-butane diisocyanate, and 1,6-hexamethylene diisocyanate. Is mentioned.
- Examples of the diisocyanate compound containing an alicyclic hydrocarbon represented by R include 1,4-cyclohexane diisocyanate and 4,4-cyclohexane diisocyanate.
- examples of the aromatic diisocyanate compound containing an aromatic hydrocarbon represented by R include 4,4′-diphenylmethane diisocyanate and tolylene diisocyanate. These can be used alone or in combination of two or more.
- P ′ is derived from a diol compound containing a short-chain aliphatic hydrocarbon, alicyclic hydrocarbon, or aromatic hydrocarbon represented by P ′.
- Examples of the aliphatic diol compound containing a short-chain aliphatic hydrocarbon represented by P ′ include glycol and polyalkylene glycol.
- Examples of the alicyclic diol compound containing an alicyclic hydrocarbon represented by P ′ include cyclopentane-1,2-diol, cyclohexane-1,2-diol, cyclohexane-1,3-diol, Examples include cyclohexane-1,4-diol and cyclohexane-1,4-dimethanol.
- examples of the aromatic diol compound containing an aromatic hydrocarbon represented by P ′ include hydroquinone, resorcin, chlorohydroquinone, bromohydroquinone, methylhydroquinone, phenylhydroquinone, methoxyhydroquinone, phenoxyhydroquinone, 4,4′- Dihydroxybiphenyl, 4,4′-dihydroxydiphenyl ether, 4,4′-dihydroxydiphenyl sulfide, 4,4′-dihydroxydiphenylsulfone, 4,4′-dihydroxybenzophenone, 4,4′-dihydroxydiphenylmethane, bisphenol A, 1, Examples include 1-di (4-hydroxyphenyl) cyclohexane, 1,2-bis (4-hydroxyphenoxy) ethane, 1,4-dihydroxynaphthalene, and 2,6-dihydroxynaphthalene. These can be used alone or in combination of two or more.
- the number average molecular weight of the polymer forming the hard segment is preferably 300 to 1500 from the viewpoint of melt moldability.
- the number average molecular weight of the polymer forming the soft segment is preferably 500 to 20000, more preferably 500 to 5000, and particularly preferably 500 to 3000, from the viewpoints of flexibility and thermal stability of the polyurethane-based thermoplastic elastomer.
- the mass ratio (x: y) of the hard segment (x) and the soft segment (y) is preferably 15:85 to 90:10, and preferably 30:70 to 90:10 from the viewpoint of moldability of the tire frame body. Is more preferable.
- the polyurethane-based thermoplastic elastomer can be synthesized by copolymerizing a polymer forming a hard segment and a polymer forming a soft segment by a known method.
- a polyurethane-based thermoplastic elastomer for example, thermoplastic polyurethane described in JP-A-5-331256 can be used.
- a combination of a hard segment composed only of an aromatic diol and an aromatic diisocyanate and a soft segment composed only of a polycarbonate ester is preferable.
- TDI isocyanate
- polyester polyol copolymer TDI / polyether polyol copolymer, TDI / caprolactone polyol copolymer, TDI / polycarbonate polyol copolymer, 4,4′-diphenylmethane diisocyanate (MDI) / Polyester polyol copolymer, MDI / polyether polyol copolymer, MDI / caprolactone polyol copolymer, MDI / polycarbonate polyol copolymer, and MDI + hydroquinone / polyhexa At least one selected from methylene carbonate copolymers is preferred.
- TDI / polyester polyol copolymer TDI / polyether polyol copolymer
- MDI / polyester polyol copolymer MDI / polyether polyol copolymer
- MDI + hydroquinone / polyhexamethylene carbonate copolymer At least one selected from is more preferable.
- thermoplastic elastomers examples include, for example, “Elastolan” series (for example, ET680, ET880, ET690, and ET890) manufactured by BASF, and “Clamiron U” series manufactured by Kuraray Co., Ltd. (For example, 2000 series, 3000 series, 8000 series, 9000 series, etc.), “Milactolan” series (for example, XN-2001, XN-2004, P390RSUP, P480RSUI, P26MRNAT, E490, E590, etc.) manufactured by Japan Miraclan Co., Ltd. And P890 etc.) can be used.
- “Elastolan” series for example, ET680, ET880, ET690, and ET890
- BASF BASF
- Clamiron U manufactured by Kuraray Co., Ltd.
- Milactolan for example, XN-2001, XN-2004, P390RSUP, P480RSUI, P26MRNAT, E490, E
- thermoplastic elastomer for example, at least a polyolefin forms a hard segment with a crystalline and high melting point, and other polymers (for example, other polyolefins and polyvinyl compounds) are amorphous and have a low glass transition temperature. Examples thereof include materials forming a soft segment. Examples of the polyolefin forming the hard segment include polyethylene, polypropylene, isotactic polypropylene, and polybutene. Examples of olefinic thermoplastic elastomers include olefin- ⁇ -olefin random copolymers, olefin block copolymers, and the like.
- propylene block copolymer ethylene-propylene copolymer, propylene-1-hexene copolymer, propylene-4-methyl-1-pentene copolymer, propylene-1-butene copolymer, ethylene- 1-hexene copolymer, ethylene-4-methyl-pentene copolymer, ethylene-1-butene copolymer, 1-butene-1-hexene copolymer, 1-butene-4-methyl-pentene, ethylene- Methacrylic acid copolymer, ethylene-methyl methacrylate copolymer, ethylene-ethyl methacrylate copolymer, ethylene-butyl methacrylate copolymer, ethylene-methyl acrylate copolymer, ethylene-ethyl acrylate copolymer, ethylene -Butyl acrylate copolymer, propylene-methacrylic acid copolymer, propylene-methacrylic Meth
- thermoplastic elastomers include propylene block copolymers, ethylene-propylene copolymers, propylene-1-hexene copolymers, propylene-4-methyl-1-pentene copolymers, propylene-1- Butene copolymer, ethylene-1-hexene copolymer, ethylene-4-methyl-pentene copolymer, ethylene-1-butene copolymer, ethylene-methacrylic acid copolymer, ethylene-methyl methacrylate copolymer , Ethylene-ethyl methacrylate copolymer, ethylene-butyl methacrylate copolymer, ethylene-methyl acrylate copolymer, ethylene-ethyl acrylate copolymer, ethylene-butyl acrylate copolymer, propylene-methacrylic acid copolymer , Propylene-methyl methacrylate copolymer, pro Lene-e
- olefin resins such as ethylene and propylene may be used.
- 50 mass% or more and 100 mass% or less of the olefin resin content rate in an olefin type thermoplastic elastomer are preferable.
- the number average molecular weight of the olefinic thermoplastic elastomer is preferably 5,000 to 10,000,000.
- the mechanical properties of the thermoplastic resin material are sufficient and the processability is excellent.
- the number average molecular weight of the olefinic thermoplastic elastomer is more preferably 7,000 to 1,000,000, and particularly preferably 10,000 to 1,000,000. Thereby, the mechanical properties and processability of the thermoplastic resin material can be further improved.
- the number average molecular weight of the polymer forming the soft segment is preferably 200 to 6000 from the viewpoint of toughness and low temperature flexibility.
- the mass ratio (x: y) of the hard segment (x) and the soft segment (y) is preferably 50:50 to 95:15, and preferably 50:50 to 90:10 from the viewpoint of moldability of the tire frame body. Is more preferable.
- the olefinic thermoplastic elastomer can be synthesized by copolymerization by a known method.
- an olefinic thermoplastic elastomer obtained by acid modification may be used as the olefinic thermoplastic elastomer.
- a product obtained by acid-modifying an olefinic thermoplastic elastomer means that an unsaturated compound having an acidic group such as a carboxylic acid group, a sulfuric acid group, and a phosphoric acid group is bonded to the olefinic thermoplastic elastomer.
- Examples of bonding an unsaturated compound having an acidic group such as a carboxylic acid group, a sulfuric acid group, and a phosphoric acid group to an olefin thermoplastic elastomer include, for example, an unsaturated compound having an acidic group as an olefin thermoplastic elastomer, Examples include bonding (for example, graft polymerization) an unsaturated bonding site of an unsaturated carboxylic acid (for example, generally maleic anhydride).
- the unsaturated compound having an acidic group is preferably an unsaturated compound having a carboxylic acid group which is a weak acid group from the viewpoint of suppressing deterioration of the olefin-based thermoplastic elastomer.
- acrylic acid, methacrylic acid, itaconic acid, croton include acids, isocrotonic acid, and maleic acid.
- thermoplastic elastomers examples include “Tuffmer” series (for example, A0550S, A1050S, A4050S, A1070S, A4070S, A35070S, A1085S, A4085S, A7090, A70090, MH7007, MH7010, manufactured by Mitsui Chemicals, Inc.
- the resin material may contain components other than the thermoplastic elastomer as desired.
- components other than the thermoplastic elastomer include rubber, thermoplastic resins, fillers (eg, silica, calcium carbonate, and clay), anti-aging agents, oils, plasticizers, color formers, and weathering agents.
- the content of the thermoplastic elastomer in the resin material is preferably 50% by mass or more from the viewpoint of sufficiently achieving the effects of the present disclosure, and is 80% by mass. More preferably, it is more preferably 90% by mass or more.
- the crystallization temperature of the thermoplastic elastomer contained in the resin material is preferably in the range of 148 ° C. to 160 ° C., more preferably in the range of 150 ° C. to 155 ° C., and in the range of 152 ° C. to 154 ° C. More preferably, it is within.
- the crystallization temperature is in the above range, the amorphous portion thickness La, the long period L, the orientation degree f, the crystallinity degree Xc, and the like can be easily controlled within the above-described ranges. In particular, the crack resistance against impact is easily improved.
- the crystallization temperature of the thermoplastic elastomer is measured by differential scanning calorimetry (DSC).
- the crystallization temperature of the thermoplastic elastomer having the highest content by mass is within the above range. Further, it is more preferable to include two or more thermoplastic elastomers having a crystallization temperature within the above range, including the thermoplastic elastomer having the highest content on a mass basis, and the crystallization temperatures of all the thermoplastic elastomers included. Is more preferably within the above range.
- the melting point of the resin material is usually about 100 ° C. to 350 ° C., but is preferably about 100 ° C. to 250 ° C., more preferably 120 ° C. to 250 ° C. from the viewpoint of tire durability and productivity.
- the tensile elastic modulus defined by JIS K7113: 1995 of the resin material (that is, the tire frame body) itself is preferably 50 MPa to 1000 MPa, more preferably 50 MPa to 800 MPa, and particularly preferably 50 MPa to 700 MPa.
- the tensile modulus of the resin material is 50 MPa to 1000 MPa, the rim can be assembled efficiently while maintaining the shape of the tire frame.
- the tensile strength specified in JIS K7113 (1995) of the resin material (that is, the tire skeleton) itself is usually about 15 MPa to 70 MPa, preferably 17 MPa to 60 MPa, and more preferably 20 MPa to 55 MPa.
- the tensile yield strength defined in JIS K7113 (1995) of the resin material (that is, the tire skeleton) itself is preferably 5 MPa or more, more preferably 5 MPa to 20 MPa, and particularly preferably 5 MPa to 17 MPa.
- the resin material can withstand deformation against a load applied to the tire during traveling.
- the tensile yield elongation defined by JIS K7113 (1995) of the resin material (that is, the tire frame body) itself is preferably 10% or more, more preferably 10% to 70%, and particularly preferably 15% to 60%.
- the tensile yield elongation of the resin material is 10% or more, the elastic region is large and the rim assembly property can be improved.
- the tensile elongation at break stipulated in JIS K7113 (1995) of the resin material (that is, the tire frame body) itself is preferably 50% or more, more preferably 100% or more, particularly preferably 150% or more, and most preferably 200% or more.
- the tensile elongation at break of the resin material is 50% or more, the rim assemblability is good, and it is difficult to break against a collision.
- the deflection temperature under load defined by ISO 75-2 or ASTM D648 of the resin material (that is, tire frame body) itself (condition: at 0.45 MPa load) is preferably 50 ° C. or higher, more preferably 50 ° C. to 150 ° C., 50 ° C. to 130 ° C. is particularly preferred.
- the deflection temperature under load of the resin material is 50 ° C. or higher, deformation of the tire skeleton can be suppressed even when vulcanization is performed in the manufacture of the tire.
- the Vicat softening temperature (Method A) defined in JIS K7206 (2016) of the resin material (that is, the tire skeleton) itself is preferably 130 ° C. or higher, preferably 130 to 250 ° C., and more preferably 130 to 220 ° C.
- the softening temperature (Method A) of the thermoplastic resin material is 130 ° C. or higher, softening and deformation of the tire in the use environment can be suppressed.
- deformation of the tire frame body can be suppressed.
- the tire according to the present embodiment may include a member other than the tire frame as necessary.
- a reinforcing member for reinforcing the tire frame body disposed on the outer periphery of the tire frame body or the like may be included.
- the reinforcing member include a cord member formed by including a metal member such as a steel cord, and a cord member coated with a coating resin material is also used.
- Examples of the resin used for the covering resin material in the reinforcing member include a thermosetting resin, a thermoplastic resin, and a thermoplastic elastomer.
- examples of the thermosetting resin include phenol resin, urea resin, melamine resin, epoxy resin, polyamide resin, and polyester resin.
- examples of the thermoplastic resin include urethane resin, olefin resin, vinyl chloride resin, polyamide resin, and polyester resin.
- thermoplastic elastomer examples include polyester-based thermoplastic elastomer (TPC), polyamide-based thermoplastic elastomer (TPA), polyolefin-based thermoplastic elastomer (TPO), and polystyrene-based thermoplastic elastomer (TPS) defined in JIS K6418: 2007. ), Polyurethane-based thermoplastic elastomer (TPU), crosslinked thermoplastic rubber (TPV), or other thermoplastic elastomer (TPZ). In view of elasticity required during running, moldability during production, and the like, it is preferable to use a thermoplastic elastomer among these. Moreover, it is preferable that the same kind of thermoplastic elastomer as the thermoplastic elastomer contained in the resin material which forms a tire frame is included.
- TPC polyester-based thermoplastic elastomer
- TPA polyamide-based thermoplastic elastomer
- TPO polyolefin-based thermoplastic elastomer
- a reinforcing member having a structure in which the cord member is coated with a coating resin material via an adhesive may be used, and the reinforcing member may be disposed on the tire frame body.
- the Martens hardness (d1) of the tire frame body, the Martens hardness (d2) of the coating resin material, and the Martens hardness (d3) of the adhesive layer satisfy the relationship of d1 ⁇ d2 ⁇ d3.
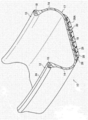
- FIG. 1A is a perspective view showing a cross section of a part of the tire 10 according to the first embodiment.
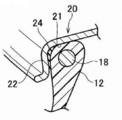
- FIG. 1B is a cross-sectional view of a bead portion when the tire 10 according to the first embodiment is mounted on a rim.
- the tire 10 has substantially the same cross-sectional shape as a rubber pneumatic tire generally used conventionally.
- FIG. 1A shows that the tire 10 has substantially the same cross-sectional shape as a rubber pneumatic tire generally used conventionally.
- the tire 10 includes a pair of bead portions 12 that contact the bead seat 21 and the rim flange 22 of the rim 20 shown in FIG. 1B, and side portions 14 that extend outward from the bead portion 12 in the tire radial direction.
- the tire case 17 includes only a crown portion 16 (that is, an outer peripheral portion) that connects an outer end in the tire radial direction of one side portion 14 and an outer end in the tire radial direction of the other side portion 14.
- the tire case 17 corresponds to the tire skeleton described above, and is formed of the resin material described above. In the first embodiment, the tire case 17 is entirely formed of the resin material described above, but the present disclosure is not limited to this configuration. Different resin materials may be used for each part of the tire case 17 (for example, the side portion 14, the crown portion 16, the bead portion 12, etc.) in the same manner as a rubber pneumatic tire that has been generally used conventionally. Further, in order to reinforce each part of the tire case 17, a reinforcing material (for example, a polymer material, a metal fiber, a cord, a nonwoven fabric, a woven fabric, or the like) may be embedded and disposed in each part of the tire case 17. Good.
- a reinforcing material for example, a polymer material, a metal fiber, a cord, a nonwoven fabric, a woven fabric, or the like
- two tire case halves that is, tire frame pieces
- the tire case 17 is not limited to the one formed by joining two members (that is, two tire case halves), and may be formed by joining three or more members.
- the tire case half can be produced by methods such as vacuum forming, pressure forming, injection molding, and melt casting. For this reason, it is not necessary to perform vulcanization compared to the case where a tire case is molded with rubber as in the prior art, the manufacturing process can be greatly simplified, and the molding time can be shortened.
- an annular bead core 18 is embedded in the bead portion 12 shown in FIG. 1B in the same manner as a conventionally used pneumatic tire.
- a steel cord is used as the bead core 18, but an organic fiber cord, a resin-coated organic fiber cord, a hard resin cord, or the like may be used.
- the bead core 18 can also be abbreviate
- the portion of the bead portion 12 that contacts the rim 20 and at least the portion that contacts the rim flange 22 of the rim 20 are made of a material that has better sealing properties than the resin material that forms the tire case 17.
- An annular seal layer 24 is formed.
- the seal layer 24 may also be formed at a portion where the bead portion 12 and the bead sheet 21 of the tire case 17 are in contact with each other. Note that the sealing layer 24 may be omitted if the sealing property between the rim 20 can be secured only with the resin material forming the tire case 17.
- Examples of the material having better sealing performance than the resin material forming the tire case 17 include materials softer than the resin material forming the tire case 17, such as rubber, thermoplastic resin and thermoplastic elastomer softer than the resin material. Can be mentioned.
- a reinforcement cord 26 having higher rigidity than the resin material forming the tire case 17 is wound around the crown portion 16 in the circumferential direction of the tire case 17.
- the reinforcing cord 26 is wound spirally in a state in which at least a part thereof is embedded in the crown portion 16 in a cross-sectional view along the axial direction of the tire case 17, thereby forming a reinforcing cord layer 28.
- a tread 30 made of a material superior in wear resistance to the resin material forming the tire case 17, for example, rubber, is disposed.
- the reinforcing cord 26 is in a state in which a metal member 26A such as a steel cord is covered with a covering resin material 27 (that is, a covering cord member).
- a metal member 26A such as a steel cord
- a covering resin material 27 that is, a covering cord member
- the same resin material as the resin material forming the tire case 17 is used as the coating resin material 27, but other thermoplastic resins or thermoplastic elastomers may be used.
- the reinforcement cord 26 is joined at a contact portion with the crown portion 16 by a method such as welding or adhesion with an adhesive.
- the reinforcing cord 26 may be a steel cord or the like that is not covered with the covering resin material 27.
- the elastic modulus of the coating resin material 27 is preferably set within a range of 0.1 to 10 times the elastic modulus of the resin material forming the tire case 17.
- the elastic modulus of the coating resin material 27 is 10 times or less than the elastic modulus of the resin material forming the tire case 17, the crown portion does not become too hard, and rim assembly is facilitated.
- the elastic modulus of the covering resin material 27 is 0.1 times or more of the elastic modulus of the resin material forming the tire case 17, the resin forming the reinforcing cord layer 28 is not too soft and has excellent in-plane shear rigidity. , Cornering power is improved.
- the reinforcing cord 26 has a substantially trapezoidal cross-sectional shape.
- the upper surface (that is, the outer surface in the tire radial direction) of the reinforcing cord 26 is denoted by reference numeral 26U
- the lower surface (that is, the inner surface in the tire radial direction) is denoted by reference numeral 26D.
- the cross-sectional shape of the reinforcing cord 26 is a substantially trapezoidal shape, but the present disclosure is not limited to this configuration.
- the reinforcing cord 26 may have any shape as long as the cross-sectional shape is a shape excluding a shape that becomes wider from the lower surface 26D side (that is, the inner side in the tire radial direction) toward the upper surface 26U side (that is, the outer side in the tire radial direction).
- the reinforcing cords 26 are arranged at intervals in the circumferential direction, a gap 28A is formed between adjacent reinforcing cords 26.
- the outer peripheral surface of the reinforcing cord layer 28 has a shape with irregularities, and the outer peripheral surface 17S of the tire case 17 in which the reinforcing cord layer 28 constitutes the outer peripheral portion also has an irregular shape.
- a fine roughened unevenness 96 is formed on the outer peripheral surface 17S (including the unevenness) of the tire case 17, and a cushion rubber 29 is bonded thereon via a bonding agent.
- the cushion rubber 29 flows into the contact surface with the reinforcing cord 26 so as to fill the rough unevenness 96.
- the above-mentioned tread 30 is joined on the cushion rubber 29 (that is, on the tire outer peripheral surface side).
- the tread 30 is formed with a tread pattern (not shown) including a plurality of grooves on the ground contact surface with the road surface in the same manner as a conventional rubber pneumatic tire.
- the tire manufacturing method according to the present embodiment will be described using the tire manufacturing method according to the first embodiment as an example.
- the tire case half is molded by injection molding or the like (molding process).
- the temperature of the resin material in this molding process for example, cylinder temperature, mold temperature, etc. in the case of injection molding, the thickness La and the length of the amorphous part of the thermoplastic elastomer contained in the tire case
- the period L, the orientation degree f, the crystallinity degree Xc, and the like can be controlled to be in the above-described ranges.
- the cylinder temperature is preferably in the range of 240 ° C.
- the mold temperature is preferably in the range of 50 ° C. to 110 ° C., more preferably in the range of 50 ° C. to 80 ° C., and further preferably in the range of 50 ° C. to 55 ° C.
- molding process influences control of the thickness La of the amorphous part of a thermoplastic elastomer, long period L, orientation degree f, crystallinity degree Xc, etc. .
- the cooling rate is preferably in the range of 140 ° C./second to 240 ° C./second, and more preferably in the range of 140 ° C./second to 230 ° C./second.
- the cooling time (that is, the time for cooling to the mold temperature) is preferably in the range of 1 second to 5 seconds, and more preferably in the range of 1 second to 1.5 seconds.
- the annular tire case halves obtained in the molding process are faced to each other and joined at the tire equatorial plane part to form a tire case (joining process).
- the tire case is not limited to the one formed by joining two members, and may be formed by joining three or more members.
- the joining will be described.
- tire case halves supported by a thin metal support ring face each other.
- a joining mold is installed so as to contact the outer peripheral surface of the abutting portion of the tire case half.
- the joining mold is configured to press the periphery of the joining portion (that is, the abutting portion) of the tire case half with a predetermined pressure.
- the periphery of the joint part of the tire case half is pressed at a temperature equal to or higher than the melting point of the resin material forming the tire case, so that the joint part is melted and the tire case halves are fused together to form a tire.
- Case 17 is formed.
- the temperature La of the amorphous part of the tire case 17, the long period L, the orientation degree f, the degree of crystallinity Xc, etc. can also be adjusted by adjusting the temperature of the resin material, for example, the temperature of the joining mold. Can be controlled to fall within the aforementioned range.
- the joining portion of the tire case half is heated using the joining mold, but the present disclosure is not limited thereto.
- the joining portion may be heated by a separately provided high-frequency heater or the like, or may be softened or melted beforehand by irradiation with hot air or infrared rays, and the tire case halves may be joined by pressing with a joining mold.
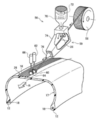
- FIG. 3 is an explanatory diagram for explaining the operation of embedding the reinforcing cord 26 in the crown portion of the tire case 17 using a cord heating device and rollers.
- the cord supply device 56 is disposed on the reel 58 around which the reinforcing cord 26 is wound, the cord heating device 59 disposed on the downstream side of the reel 58 in the cord transport direction, and the downstream side of the reinforcing cord 26 in the transport direction.
- the first roller 60, the first cylinder device 62 that moves the first roller 60 in the direction of contacting and separating from the outer peripheral surface of the tire, and the downstream side in the conveying direction of the reinforcing cord 26 of the first roller 60 A second roller 64, and a second cylinder device 66 that moves the second roller 64 in a direction in which the second roller 64 comes into contact with and separates from the tire outer peripheral surface.
- the second roller 64 can be used as a metal cooling roller.
- the surface of the first roller 60 or the second roller 64 is subjected to treatment (for example, fluororesin coating) for suppressing adhesion of the molten or softened coating resin material 27. .
- the present invention is not limited to this mode, and the roller itself may be formed of a material to which the coating resin material 27 is difficult to adhere.
- the cord supply device 56 includes the two rollers of the first roller 60 and the second roller 64.
- the present invention is not limited to this mode, and only one of the rollers is provided. You may do it.
- the cord heating device 59 includes a heater 70 and a fan 72 that generate hot air.
- the cord heating device 59 also includes a heating box 74 through which the reinforcing cord 26 passes and an outlet 76 through which the heated reinforcing cord 26 is discharged through an internal space in which hot air is supplied.
- the temperature of the heater 70 of the cord heating device 59 is raised, and the ambient air heated by the heater 70 is sent to the heating box 74 by the wind generated by the rotation of the fan 72.
- the reinforcing cord 26 unwound from the reel 58 is sent into a heating box 74 in which the internal space is heated with hot air and heated.
- the heating temperature is set to a temperature at which the covering resin material 27 of the reinforcing cord 26 is melted or softened.
- the heated reinforcing cord 26 passes through the discharge port 76 and is wound spirally around the outer peripheral surface of the crown portion 16 of the tire case 17 rotating in the direction of arrow R in FIG. At this time, the lower surface 26 ⁇ / b> D of the reinforcing cord 26 contacts the outer peripheral surface of the crown portion 16.
- the coating resin material 27 melted or softened by heating spreads on the outer peripheral surface of the crown portion 16, and the reinforcing cord 26 is welded to the outer peripheral surface of the crown portion 16. Thereby, the joint strength between the crown portion 16 and the reinforcing cord 26 is improved.
- the reinforcing cord 26 is joined to the outer peripheral surface of the crown portion 16 as described above.
- the invention is not limited to this aspect, and the joining may be performed by other methods.
- joining may be performed so that a part or the whole of the reinforcing cord 26 is embedded in the crown portion 16.
- a blasting device (not shown) emits a projection material at a high speed toward the outer peripheral surface 17S while rotating the tire case 17 side toward the outer peripheral surface 17S of the tire case 17.
- the ejected projection material collides with the outer peripheral surface 17S, and fine roughening unevenness 96 having an arithmetic average roughness Ra of 0.05 mm or more is formed on the outer peripheral surface 17S.
- the outer peripheral surface 17S becomes hydrophilic, and the wettability of the bonding agent described later is improved.
- a bonding agent for bonding the cushion rubber 29 is applied to the outer peripheral surface 17S of the tire case 17 subjected to the roughening treatment.
- the bonding agent is not particularly limited, and a triazine thiol adhesive, a chlorinated rubber adhesive, a phenolic resin adhesive, an isocyanate adhesive, a halogenated rubber adhesive, a rubber adhesive, or the like can be used. However, it is preferable to react at a temperature at which the cushion rubber 29 can be vulcanized (eg, 90 ° C. to 140 ° C.).
- the unvulcanized cushion rubber 29 is wound around the outer peripheral surface 17S to which the bonding agent has been applied for one round, and a bonding agent such as a rubber cement composition is applied onto the cushion rubber 29.
- a bonding agent such as a rubber cement composition
- the vulcanized or semi-cured tread rubber 30A is wound on the cushion rubber 29 to which the bonding agent has been applied for one round to form a raw tire case.
- the raw tire case is accommodated in a vulcanizing can or mold and vulcanized.
- the unvulcanized cushion rubber 29 flows into the roughened irregularities 96 formed on the outer peripheral surface 17S of the tire case 17 by the roughening treatment.
- the anchor rubber is exerted by the cushion rubber 29 flowing into the roughened unevenness 96, and the bonding strength between the tire case 17 and the cushion rubber 29 is improved. That is, the bonding strength between the tire case 17 and the tread 30 is improved via the cushion rubber 29.
- the tire skeleton body is formed of a resin material including a thermoplastic elastomer
- a tire is provided in which the amorphous portion has a thickness La in the range of 12.3 nm to 13.9 nm as measured by the small-angle X-ray scattering method of the thermoplastic elastomer.
- the first aspect is such that the long period L measured by the small-angle X-ray scattering method of the thermoplastic elastomer is in the range of 15.6 nm to 17.1 nm. Tires are provided.
- the degree of orientation f of the thermoplastic elastomer measured by a small angle X-ray scattering method is in the range of ⁇ 0.08 to 0.08.
- a tire according to a second aspect is provided.
- a fourth aspect of the present disclosure there is provided a tire according to any one of the first to third aspects, wherein the thermoplastic elastomer is a polyester-based thermoplastic elastomer.
- tires having the configuration shown in the first embodiment described above were produced by a known method.
- a resin material for forming the tire skeleton a polyester-based thermoplastic elastomer whose hard segment is polyester and whose soft segment is polyether is used.
- multifilaments having an average diameter of 1.15 mm (specifically, five monofilaments having an average diameter of 0.35 mm (made of steel, strength: 280 N, elongation: 3%)) were twisted.
- a heat-melted acid-modified polypropylene was adhered to the stranded wire to form an adhesive layer.
- the upper surface of the adhesive layer was covered with a polyamide-based thermoplastic elastomer extruded by an extruder (trade name “XPA9055” manufactured by UBE Co., Ltd.) and cooled to prepare a reinforcing cord.
- amorphous part thickness La, long period L, orientation degree f, and crystallinity degree Xc Using a sample prepared from the tire case of the prepared tire, the amorphous part thickness La and long period of the thermoplastic elastomer L and the degree of orientation f were measured by a small angle X-ray scattering method, and the crystallinity Xc was measured by a wide angle X-ray scattering method.
- product name: Nano-Viewer manufactured by Rigaku Corporation was used, and the measurement conditions were adjusted as follows. -Measurement condition- -Room temperature measurement-X-ray irradiation time 30 minutes Table 1 shows the measurement results.
- thermoplastic elastomer of Table 1 The detail of the thermoplastic elastomer of Table 1 is shown below.
- Hytrel 5557 polyyester-based thermoplastic elastomer, manufactured by Toray DuPont Co., Ltd., crystallization temperature: 163 ° C.
- Hytrel 4767N polyyester thermoplastic elastomer, manufactured by Toray DuPont Co., Ltd., crystallization temperature: 155 ° C.
- Example 6 Hytrel 5557 and Hytrel 4767N were mixed and used at a mass ratio of “25/75”.
- the tire of the example having the tire case formed using the thermoplastic elastomer having the amorphous portion thickness La in the range of 12.3 nm to 13.9 nm has the thickness of the amorphous portion. It turns out that it is excellent in durability compared with the tire of the comparative example which has the tire case formed using the thermoplastic elastomer which La does not exist in the said range.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Health & Medical Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Organic Chemistry (AREA)
- Tires In General (AREA)
Abstract
熱可塑性エラストマーを含む樹脂材料で形成されたタイヤ骨格体を有し、前記熱可塑性エラストマーの小角X線散乱法により測定される非晶部の厚みLaが12.3nm~13.9nmの範囲内であるタイヤ。
Description
本開示は、タイヤに関する。
従来、乗用車等の車両に用いられる空気入りタイヤにおいて、軽量化や、成形の容易さ、リサイクルのしやすさから、樹脂材料、特に熱可塑性樹脂や熱可塑性エラストマーなどを材料として用いたタイヤが検討されている。これら熱可塑性の高分子材料(つまり熱可塑性樹脂)は、射出成形が可能であるなど、生産性の向上の観点から有利な点が多い。
例えば、熱可塑性樹脂材料で形成され、環状のタイヤ骨格体を有するタイヤであって、タイヤ骨格体の外周部に周方向に巻回されて補強コード層を形成する補強コード部材を有し、熱可塑性樹脂材料が少なくともポリエステル系熱可塑性エラストマーを含むタイヤが提案されている(特許文献1参照)。
〔特許文献1〕特開2012-046025号公報
樹脂材料を用いて製造されるタイヤ骨格体では、製造後のタイヤにおける樹脂材料の状態がタイヤ骨格体の状態に影響する。従って、樹脂材料の状態を適切に制御することができれば、タイヤ骨格体、ひいてはタイヤの特性(例えば耐久性等)を所望の状態に改良できると考えられる。しかしながら、樹脂材料の状態をどのような観点から制御すれば所望の特性が実現されるかについては、いまだ検討の余地がある。
本開示は、上記事情に鑑み、樹脂材料に含まれる樹脂として熱可塑性エラストマーを含むタイヤ骨格体を有し、かつ耐久性に優れるタイヤを提供することを目的とする。
前記課題は、以下の本開示により解決される。
<1> 熱可塑性エラストマーを含む樹脂材料で形成されたタイヤ骨格体を有し、
前記熱可塑性エラストマーの小角X線散乱法により測定される非晶部の厚みLaが12.3nm~13.9nmの範囲内であるタイヤ。
前記熱可塑性エラストマーの小角X線散乱法により測定される非晶部の厚みLaが12.3nm~13.9nmの範囲内であるタイヤ。
本開示によれば、樹脂材料に含まれる樹脂として熱可塑性エラストマーを含むタイヤ骨格体を有し、かつ耐久性に優れるタイヤを提供することができる。
以下、本開示の具体的な実施形態について詳細に説明する。ただし、本開示は、以下の実施形態に何ら限定されるものではなく、本開示の目的の範囲内において、適宜変更を加えて実施することができる。
本明細書において「樹脂」とは、熱可塑性樹脂、熱可塑性エラストマー及び熱硬化性樹脂を含む概念であり、加硫ゴムは含まない。また、以下の樹脂の説明において「同種」とは、エステル系同士、スチレン系同士等、樹脂の主鎖を構成する骨格と共通する骨格を備えたものを意味する。
本明細書において「熱可塑性エラストマー」とは、結晶性で融点の高いハードセグメント、又は高い凝集力のハードセグメントを構成するポリマーと、非晶性でガラス転移温度の低いソフトセグメントを構成するポリマーと、を有する共重合体からなる高分子化合物を意味する。なお、熱可塑性エラストマーは、温度上昇とともに材料が軟化して流動し、冷却すると比較的硬く強度のある状態になる。また、熱可塑性エラストマーは、ゴム状弾性を有する高分子化合物である。
また本明細書において、「ハードセグメント」とは、相対的にソフトセグメントよりも硬い成分を指し、「ソフトセグメント」とは、相対的にハードセグメントよりも柔らかい成分を指す。なお、ハードセグメントは、塑性変形を防止する架橋ゴムの架橋点の役目を果たす分子拘束成分であることが好ましい。また、ソフトセグメントは、ゴム弾性を示す柔軟性成分であることが好ましい。
本明細書において「~」を用いて表される数値範囲は、「~」の前後に記載される数値を下限値及び上限値として含む範囲を意味する。
本明細書において「工程」との語には、独立した工程だけではなく、他の工程と明確に区別できない場合であっても、その目的が達成されるものであれば、当該工程も本用語に含まれる。
本明細書において「熱可塑性エラストマー」とは、結晶性で融点の高いハードセグメント、又は高い凝集力のハードセグメントを構成するポリマーと、非晶性でガラス転移温度の低いソフトセグメントを構成するポリマーと、を有する共重合体からなる高分子化合物を意味する。なお、熱可塑性エラストマーは、温度上昇とともに材料が軟化して流動し、冷却すると比較的硬く強度のある状態になる。また、熱可塑性エラストマーは、ゴム状弾性を有する高分子化合物である。
また本明細書において、「ハードセグメント」とは、相対的にソフトセグメントよりも硬い成分を指し、「ソフトセグメント」とは、相対的にハードセグメントよりも柔らかい成分を指す。なお、ハードセグメントは、塑性変形を防止する架橋ゴムの架橋点の役目を果たす分子拘束成分であることが好ましい。また、ソフトセグメントは、ゴム弾性を示す柔軟性成分であることが好ましい。
本明細書において「~」を用いて表される数値範囲は、「~」の前後に記載される数値を下限値及び上限値として含む範囲を意味する。
本明細書において「工程」との語には、独立した工程だけではなく、他の工程と明確に区別できない場合であっても、その目的が達成されるものであれば、当該工程も本用語に含まれる。
<タイヤ>
本実施形態に係るタイヤは、熱可塑性エラストマーを含む樹脂材料で形成された(つまり一部又は全部が樹脂材料のみにより形成された)タイヤ骨格体を有する。そして、熱可塑性エラストマーの小角X線散乱法により測定される非晶部の厚みLaが12.3nm~13.9nmの範囲内である。
本実施形態に係るタイヤは、熱可塑性エラストマーを含む樹脂材料で形成された(つまり一部又は全部が樹脂材料のみにより形成された)タイヤ骨格体を有する。そして、熱可塑性エラストマーの小角X線散乱法により測定される非晶部の厚みLaが12.3nm~13.9nmの範囲内である。
本発明者らの検討により、非晶部の厚みLaが上記範囲内にある熱可塑性エラストマーを用いて形成したタイヤ骨格体を有するタイヤは、非晶部の厚みLaが上記範囲内にない熱可塑性エラストマーのみを用いて形成したタイヤ骨格体を有するタイヤに比べて、耐久性(特に、耐亀裂性)に優れることが明らかとなった。
・非晶部の厚みLa
本明細書において熱可塑性エラストマーの非晶部の厚みLaは、熱可塑性エラストマーのハードセグメントの結晶部と非晶部との繰り返し構造における、1つの非晶部の厚みである。本明細書において非晶部の厚みLaは、タイヤ骨格体から採取した試料、又はタイヤ骨格体の形成に用いる樹脂材料から作製した試料を用いて、小角X線散乱法により下記のようにして測定される。
長周期Lを2π/qmaxと定義する。ただし、前記qmaxは、小角X線散乱の一次ピークを示すところの波数q[nm-1]である。また、結晶部の厚みをLcとする。このLcは、後述する一次元自己相関関数γ(r)の初期傾きを示す関数と最小値を示す関数の交点から算出できる。これらを用いると、非晶部の厚みLaは「La=L-Lc」のように定義される。
本明細書において熱可塑性エラストマーの非晶部の厚みLaは、熱可塑性エラストマーのハードセグメントの結晶部と非晶部との繰り返し構造における、1つの非晶部の厚みである。本明細書において非晶部の厚みLaは、タイヤ骨格体から採取した試料、又はタイヤ骨格体の形成に用いる樹脂材料から作製した試料を用いて、小角X線散乱法により下記のようにして測定される。
長周期Lを2π/qmaxと定義する。ただし、前記qmaxは、小角X線散乱の一次ピークを示すところの波数q[nm-1]である。また、結晶部の厚みをLcとする。このLcは、後述する一次元自己相関関数γ(r)の初期傾きを示す関数と最小値を示す関数の交点から算出できる。これらを用いると、非晶部の厚みLaは「La=L-Lc」のように定義される。
非晶部の厚みLaが上記の範囲内である熱可塑性エラストマーを用いて形成したタイヤ骨格体を有するタイヤは、耐久性に優れている。その理由は明らかではないが、以下のように推察される。
非晶部の厚みLaが12.3nm以上であることは、ハードセグメントの結晶部と非晶部との繰り返し構造において、非晶部の分子鎖が伸びていることを示していると考えられる。これにより、非晶部の分子鎖の配向性(つまり整列の度合)が向上する。その結果、熱可塑性エラストマーの緩衝性が高められ、タイヤの耐久性、特に衝撃に対する耐亀裂性が向上するものと考えられる。
一方、非晶部の厚みLaが13.9nm以下であることは、ハードセグメントの結晶部と非晶部との繰り返し構造において、非晶部の分子鎖が伸び過ぎていないことを示していると考えられる。そのため、伸び過ぎによる非晶部の分子鎖の強度の低下が抑制される。これにより、熱可塑性エラストマーの強度が確保され、タイヤの耐久性、特に衝撃に対する耐亀裂性が向上するものと考えられる。
非晶部の厚みLaが12.3nm以上であることは、ハードセグメントの結晶部と非晶部との繰り返し構造において、非晶部の分子鎖が伸びていることを示していると考えられる。これにより、非晶部の分子鎖の配向性(つまり整列の度合)が向上する。その結果、熱可塑性エラストマーの緩衝性が高められ、タイヤの耐久性、特に衝撃に対する耐亀裂性が向上するものと考えられる。
一方、非晶部の厚みLaが13.9nm以下であることは、ハードセグメントの結晶部と非晶部との繰り返し構造において、非晶部の分子鎖が伸び過ぎていないことを示していると考えられる。そのため、伸び過ぎによる非晶部の分子鎖の強度の低下が抑制される。これにより、熱可塑性エラストマーの強度が確保され、タイヤの耐久性、特に衝撃に対する耐亀裂性が向上するものと考えられる。
非晶部の厚みLaは、さらに12.5nm~13.7nmの範囲内であることが好ましく、12.8nm~13.4nmの範囲内であることがより好ましい。
熱可塑性エラストマーの非晶部の厚みLaの値を制御する方法は、特に制限されない。例えば、タイヤ骨格体形成時の加熱温度(例えば射出成形時のシリンダ温度や金型温度)を上げることで、非晶部の厚みLaの値を小さくすることができる。一方、タイヤ骨格体形成時の加熱温度(例えばシリンダ温度や金型温度)を下げることで、非晶部の厚みLaの値を大きくすることができる。
・長周期L
本実施形態に係るタイヤは、タイヤ骨格体に含まれる熱可塑性エラストマーの小角X線散乱法により測定される長周期Lが15.6nm~17.1nmの範囲内であることが好ましい。
本実施形態に係るタイヤは、タイヤ骨格体に含まれる熱可塑性エラストマーの小角X線散乱法により測定される長周期Lが15.6nm~17.1nmの範囲内であることが好ましい。
本明細書において熱可塑性エラストマーの長周期Lは、熱可塑性エラストマーにおけるハードセグメントの結晶部と非晶部の繰り返し構造において、1つの結晶部と1つの非晶部とからなる繰り返し単位における結晶部の厚みと非晶部の厚みとの合計値である。本明細書において長周期Lは、タイヤ骨格体から採取した試料、又はタイヤ骨格体の形成に用いる樹脂材料から作製した試料を用いて、小角X線散乱法により下記のようにして算出される。
一次元自己相関関数の値から得られた一次元自己相関関数γ(r)をrに対してプロットし、その一次ピークを取るrの値とする。式中の「q」は、小角X線散乱の一次ピークを示すところの波数[nm-1]を表す。「r」は、ポリマー空間中の任意の点で、距離の次元を持つ。「I(q)」は、X線散乱強度を表す。
一次元自己相関関数γ(r)=(∫I(q)q2cos(rq)dq)/(∫I(q)q2dq)
一次元自己相関関数の値から得られた一次元自己相関関数γ(r)をrに対してプロットし、その一次ピークを取るrの値とする。式中の「q」は、小角X線散乱の一次ピークを示すところの波数[nm-1]を表す。「r」は、ポリマー空間中の任意の点で、距離の次元を持つ。「I(q)」は、X線散乱強度を表す。
一次元自己相関関数γ(r)=(∫I(q)q2cos(rq)dq)/(∫I(q)q2dq)
長周期Lが上記範囲内であることで、タイヤの耐久性、特に衝撃に対する耐亀裂性が向上する。これは、長周期Lが15.6nm以上であることで、分子同士の擦れが軽減されてタイヤの耐久性が向上するためと考えられる。また、17.1nm以下であることで、分子鎖の伸び過ぎによる高弾性率化が抑えられ、この観点からもタイヤの耐久性が向上するためと考えられる。
長周期Lは、さらに15.8nm~17.0nmの範囲内であることが好ましく、16.1nm~16.7nmの範囲内であることがより好ましい。
長周期Lの値は、熱可塑性エラストマー中の非晶部の厚みLaが大きくなるほど大きくなる。また、熱可塑性エラストマー中の結晶部の成長が促進され結晶部の厚みが増大するほど大きくなる。なお、長周期Lが大きくなるほど、熱可塑性エラストマーの融点が高くなる傾向にある。
熱可塑性エラストマーの長周期Lの値を制御する方法は、特に制限されない。例えば、前述の通り非晶部の厚みLaの値を制御する方法が挙げられる。また、タイヤ骨格体形成時の加熱温度(例えばシリンダ温度や金型温度)を上げて冷却に要する時間を長くして、結晶の成長を促すことで、長周期Lを大きくすることができる。一方、タイヤ骨格体形成時の加熱温度(例えばシリンダ温度や金型温度)を下げて冷却に要する時間を短くして、結晶の成長を抑制することで、長周期Lを小さくすることができる。
・配向度f
本実施形態に係るタイヤは、タイヤ骨格体に含まれる熱可塑性エラストマーの小角X線散乱法により測定される配向度fが-0.08~0.08の範囲内である(つまり配向度fの絶対値が0以上0.08以下である)ことが好ましい。
本実施形態に係るタイヤは、タイヤ骨格体に含まれる熱可塑性エラストマーの小角X線散乱法により測定される配向度fが-0.08~0.08の範囲内である(つまり配向度fの絶対値が0以上0.08以下である)ことが好ましい。
本明細書において熱可塑性エラストマーの配向度fは、熱可塑性エラストマー中のハードセグメントの結晶部における分子の配向度を意味する。なお、配向度fの絶対値が小さいほど分子の配向の状態が、よりランダムである。本明細書において配向度fは、タイヤ骨格体から採取した試料、又はタイヤ骨格体の形成に用いる樹脂材料から作製した試料を用いて、小角X線散乱法により結晶配向角を測定し、下記式によって導き出される値である。式中の「θ」は結晶配向角を表す。
f=1/2×(3×<cos2θ>-1)
f=1/2×(3×<cos2θ>-1)
配向度fが-0.08~0.08の範囲内であることで、タイヤの耐久性、特に衝撃に対する耐亀裂性が向上する。これは、配向度fを上記の範囲内とすることで、走行中におけるタイヤ骨格体への力学的入力を効果的に分散させることができ、力学強度が高まるためと推測される。
配向度fは、さらに-0.08~0.04の範囲内であることが好ましく、-0.02~0.02の範囲内であることがより好ましい。
熱可塑性エラストマーの配向度fの値を制御する方法は、特に制限されない。例えば、タイヤ骨格体形成の際の射出成形時の熱可塑性エラストマーの温度、シリンダ温度や金型温度、及び冷却速度等を変化させることで行うことができる。例えば、熱可塑性エラストマーの射出成形時の温度を高くする(すなわち、熱可塑性エラストマーの温度を上げる)ことで粘度を下げ、シリンダ温度や金型温度を上げて冷却に要する時間を長くして、分子運動を緩和させることで、配向度fを小さくすることができる。
・結晶化度Xc
本実施形態に係るタイヤは、タイヤ骨格体に含まれる熱可塑性エラストマーの広角X線散乱法により測定される結晶化度Xcが12%~45%の範囲内であることが好ましい。
本実施形態に係るタイヤは、タイヤ骨格体に含まれる熱可塑性エラストマーの広角X線散乱法により測定される結晶化度Xcが12%~45%の範囲内であることが好ましい。
本明細書において熱可塑性エラストマーの結晶化度Xcは、熱可塑性エラストマーのハードセグメントにおける結晶部の割合を表す。なお、結晶化度Xcの値が大きいほど結晶部の割合が大きく、非晶部の割合が小さい。本明細書において結晶化度Xcは、タイヤ骨格体から採取した試料、又はタイヤ骨格体の形成に用いる樹脂材料から作製した試料を用いて、広角X線散乱法により結晶の散乱強度面積と非晶の散乱強度面積とを求め、下記の計算式にて導き出される値である。
Xc(%)=(結晶の散乱強度面積)/(結晶の散乱強度面積+非晶の散乱強度面積)×100
Xc(%)=(結晶の散乱強度面積)/(結晶の散乱強度面積+非晶の散乱強度面積)×100
結晶化度Xcが12%~45%の範囲内であることで、タイヤの耐久性、特に衝撃に対する耐亀裂性が向上する。これは、結晶化度Xcが12%以上であると、高耐熱化するためと推測される。また、結晶化度Xcが45%以下であると、結晶起点による破壊現象が抑えられるためと推測される。
結晶化度Xcは、12%~37%であることがさらに好ましい。
熱可塑性エラストマーの結晶化度Xcの値を制御する方法は特に制限されない。例えば、タイヤ骨格体形成時の加熱温度(例えばシリンダ温度や金型温度)を上げて冷却に要する時間を長くして、結晶の成長を促すことで、結晶化度Xcを大きくすることができる。一方、冷却中の金型温度を下げて冷却に要する時間を短くして、結晶の成長を抑制することで、結晶化度Xcを小さくすることができる。
[樹脂材料]
樹脂材料は、熱可塑性エラストマーを含み、また所望により、添加剤等の熱可塑性エラストマー以外の成分を含んでもよい。
タイヤ骨格体の形成に用いる熱可塑性エラストマーの種類は、特に制限されない。例えば、ポリエステル系熱可塑性エラストマー(TPC)、ポリアミド系熱可塑性エラストマー(TPA)、ポリスチレン系熱可塑性エラストマー(TPS)、ポリウレタン系熱可塑性エラストマー(TPU)、オレフィン系熱可塑性エラストマー(TPO)、熱可塑性ゴム架橋体(TPV)、及びその他の熱可塑性エラストマー(TPZ)等が挙げられる。熱可塑性エラストマーの定義及び分類については、JIS K6418を参照することができる。
樹脂材料は、熱可塑性エラストマーを含み、また所望により、添加剤等の熱可塑性エラストマー以外の成分を含んでもよい。
タイヤ骨格体の形成に用いる熱可塑性エラストマーの種類は、特に制限されない。例えば、ポリエステル系熱可塑性エラストマー(TPC)、ポリアミド系熱可塑性エラストマー(TPA)、ポリスチレン系熱可塑性エラストマー(TPS)、ポリウレタン系熱可塑性エラストマー(TPU)、オレフィン系熱可塑性エラストマー(TPO)、熱可塑性ゴム架橋体(TPV)、及びその他の熱可塑性エラストマー(TPZ)等が挙げられる。熱可塑性エラストマーの定義及び分類については、JIS K6418を参照することができる。
これらの中でも熱可塑性エラストマーとしては、耐屈曲疲労性が他の熱可塑性エラストマーに比べて高いとの利点から、ポリエステル系熱可塑性エラストマーが好ましい。ポリエステル系熱可塑性エラストマーを含むタイヤは、その高い耐屈曲疲労性により、繰り返し加えられる屈曲に対して疲労亀裂の発生や成長が抑制されて、高い耐久性を示す。
-ポリエステル系熱可塑性エラストマー-
ポリエステル系熱可塑性エラストマーは、弾性を有する高分子化合物であり、結晶性で融点の高いハードセグメントを形成するポリエステルを含むポリマーと、非晶性でガラス転移温度の低いソフトセグメントを形成するポリマーと、を有する共重合体からなる熱可塑性樹脂材料である。そして、ポリエステル系熱可塑性エラストマーとは、その構造中にポリエステルからなる部分構造を有するものを意味する。ポリエステル系熱可塑性エラストマーとしては、例えば、JIS K6418:2007に規定されるエステル系熱可塑性エラストマー(TPC)等が挙げられる。
ポリエステル系熱可塑性エラストマーとしては、例えば、少なくともポリエステルが結晶性で融点の高いハードセグメントを形成し、他のポリマー(例えば、ポリエステル又はポリエーテル等)が非晶性でガラス転移温度の低いソフトセグメントを形成している材料が挙げられる。
ポリエステル系熱可塑性エラストマーは、弾性を有する高分子化合物であり、結晶性で融点の高いハードセグメントを形成するポリエステルを含むポリマーと、非晶性でガラス転移温度の低いソフトセグメントを形成するポリマーと、を有する共重合体からなる熱可塑性樹脂材料である。そして、ポリエステル系熱可塑性エラストマーとは、その構造中にポリエステルからなる部分構造を有するものを意味する。ポリエステル系熱可塑性エラストマーとしては、例えば、JIS K6418:2007に規定されるエステル系熱可塑性エラストマー(TPC)等が挙げられる。
ポリエステル系熱可塑性エラストマーとしては、例えば、少なくともポリエステルが結晶性で融点の高いハードセグメントを形成し、他のポリマー(例えば、ポリエステル又はポリエーテル等)が非晶性でガラス転移温度の低いソフトセグメントを形成している材料が挙げられる。
ハードセグメントを形成するポリエステルとしては、例えば芳香族ポリエステルを用いることができる。芳香族ポリエステルは、例えば、芳香族ジカルボン酸又はそのエステル形成性誘導体と、脂肪族ジオールと、から形成することができる。
芳香族ポリエステルは、例えば、テレフタル酸及び/又はジメチルテレフタレートと、1,4-ブタンジオールと、から誘導されるポリブチレンテレフタレートが挙げられる。更に、イソフタル酸、フタル酸、ナフタレン-2,6-ジカルボン酸、ナフタレン-2,7-ジカルボン酸、ジフェニル-4,4’-ジカルボン酸、ジフェノキシエタンジカルボン酸、5-スルホイソフタル酸、又はこれらのエステル形成性誘導体等のジカルボン酸成分と、分子量300以下のジオール(例えば、エチレングリコール、トリメチレングリコール、ペンタメチレングリコール、ヘキサメチレングリコール、ネオペンチルグリコール、及びデカメチレングリコール等の脂肪族ジオール、1,4-シクロヘキサンジメタノール、及びトリシクロデカンジメチロール等の脂環式ジオール、並びにキシリレングリコール、ビス(p-ヒドロキシ)ジフェニル、ビス(p-ヒドロキシフェニル)プロパン、2,2-ビス[4-(2-ヒドロキシエトキシ)フェニル]プロパン、ビス[4-(2-ヒドロキシ)フェニル]スルホン、1,1-ビス[4-(2-ヒドロキシエトキシ)フェニル]シクロヘキサン、4,4’-ジヒドロキシ-p-ターフェニル、及び4,4’-ジヒドロキシ-p-クオーターフェニル等の芳香族ジオール)等のジオール成分と、から誘導されるポリエステルであってもよい。或いは、これらのジカルボン酸成分及びジオール成分を2種以上併用した共重合ポリエステルであってもよい。また、3官能以上の多官能カルボン酸成分、多官能オキシ酸成分、多官能ヒドロキシ成分等を5モル%以下の範囲で共重合することも可能である。
ハードセグメントを形成するポリエステルとしては、例えば、ポリエチレンテレフタレート、ポリブチレンテレフタレート、ポリメチレンテレフタレート、ポリエチレンナフタレート、及びポリブチレンナフタレート等が挙げられる。中でも、ポリブチレンテレフタレートが好ましい。
ハードセグメントを形成するポリエステルとしては、例えば、ポリエチレンテレフタレート、ポリブチレンテレフタレート、ポリメチレンテレフタレート、ポリエチレンナフタレート、及びポリブチレンナフタレート等が挙げられる。中でも、ポリブチレンテレフタレートが好ましい。
また、ソフトセグメントを形成するポリマーとしては、例えば、脂肪族ポリエステル、及び脂肪族ポリエーテル等が挙げられる。
脂肪族ポリエーテルとしては、ポリ(エチレンオキシド)グリコール、ポリ(プロピレンオキシド)グリコール、ポリ(テトラメチレンオキシド)グリコール、ポリ(ヘキサメチレンオキシド)グリコール、エチレンオキシドとプロピレンオキシドとの共重合体、ポリ(プロピレンオキシド)グリコールのエチレンオキシド付加重合体、及びエチレンオキシドとテトラヒドロフランとの共重合体等が挙げられる。
脂肪族ポリエステルとしては、ポリ(ε-カプロラクトン)、ポリエナントラクトン、ポリカプリロラクトン、ポリブチレンアジペート、及びポリエチレンアジペート等が挙げられる。
脂肪族ポリエーテルとしては、ポリ(エチレンオキシド)グリコール、ポリ(プロピレンオキシド)グリコール、ポリ(テトラメチレンオキシド)グリコール、ポリ(ヘキサメチレンオキシド)グリコール、エチレンオキシドとプロピレンオキシドとの共重合体、ポリ(プロピレンオキシド)グリコールのエチレンオキシド付加重合体、及びエチレンオキシドとテトラヒドロフランとの共重合体等が挙げられる。
脂肪族ポリエステルとしては、ポリ(ε-カプロラクトン)、ポリエナントラクトン、ポリカプリロラクトン、ポリブチレンアジペート、及びポリエチレンアジペート等が挙げられる。
これらの脂肪族ポリエーテル及び脂肪族ポリエステルの中でも、得られるポリエステルブロック共重合体の弾性特性の観点から、ソフトセグメントを形成するポリマーとしては、ポリ(テトラメチレンオキシド)グリコール、ポリ(プロピレンオキシド)グリコールのエチレンオキシド付加物、ポリ(ε-カプロラクトン)、ポリブチレンアジペート、及びポリエチレンアジペート等が好ましい。
ハードセグメントを形成するポリマー(つまりポリエステル)の数平均分子量は、強靱性及び低温柔軟性の観点から、300~6000が好ましい。
また、ソフトセグメントを形成するポリマーの数平均分子量は、強靱性及び低温柔軟性の観点から、300~6000が好ましい。
さらに、ハードセグメント(x)とソフトセグメント(y)との質量比(x:y)は、タイヤ骨格体の成形性の観点から、99:1~20:80が好ましく、98:2~30:70が更に好ましい。
また、ソフトセグメントを形成するポリマーの数平均分子量は、強靱性及び低温柔軟性の観点から、300~6000が好ましい。
さらに、ハードセグメント(x)とソフトセグメント(y)との質量比(x:y)は、タイヤ骨格体の成形性の観点から、99:1~20:80が好ましく、98:2~30:70が更に好ましい。
上述のハードセグメントとソフトセグメントとの組合せとしては、例えば、上述で挙げたハードセグメントとソフトセグメントとのそれぞれの組合せを挙げることができる。これらの中でも、上述のハードセグメントとソフトセグメントとの組合せとしては、ハードセグメントがポリブチレンテレフタレートであり、ソフトセグメントが脂肪族ポリエーテルである組み合わせが好ましく、ハードセグメントがポリブチレンテレフタレートであり、ソフトセグメントがポリ(エチレンオキシド)グリコールである組み合わせが更に好ましい。
ポリエステル系熱可塑性エラストマーの市販品としては、例えば、東レ・デュポン(株)製の「ハイトレル」シリーズ(例えば、3046、5557、6347、4047N、及び4767N等)、東洋紡(株)製の「ペルプレン」シリーズ(例えば、P30B、P40B、P40H、P55B、P70B、P150B、P280B、E450B、P150M、S1001、S2001、S5001、S6001、及びS9001等)等を用いることができる。
ポリエステル系熱可塑性エラストマーは、ハードセグメントを形成するポリマー及びソフトセグメントを形成するポリマーを公知の方法によって共重合することで合成することができる。
また、本実施形態において樹脂材料中にポリエステル系熱可塑性エラストマーを含む場合、含まれる全熱可塑性エラストマーに占めるポリエステル系熱可塑性エラストマーの含有率は、特に限定されるものではないが、全樹脂の総量に対して50質量%以上が好ましく、80質量%以上がより好ましく、90質量%以上がさらに好ましい。ポリエステル系熱可塑性エラストマーの含有率が、熱可塑性エラストマーの総量に対して、50質量%以上であるとポリエステル系熱可塑性エラストマーの特性を十分に発揮させることができ、タイヤの耐久性をより向上させ易くなる。
-ポリアミド系熱可塑性エラストマー-
ポリアミド系熱可塑性エラストマーとは、結晶性で融点の高いハードセグメントを形成するポリマーと、非晶性でガラス転移温度の低いソフトセグメントを形成するポリマーと、を有する共重合体からなる熱可塑性の樹脂材料であって、前記ハードセグメントを形成するポリマーの主鎖にアミド結合(-CONH-)を有するものを意味する。
ポリアミド系熱可塑性エラストマーとしては、例えば、少なくともポリアミドが結晶性で融点の高いハードセグメントを形成し、他のポリマー(例えば、ポリエステル、又はポリエーテル等)が非晶性でガラス転移温度の低いソフトセグメントを形成している材料が挙げられる。また、ポリアミド系熱可塑性エラストマーは、ハードセグメント及びソフトセグメントの他に、ジカルボン酸等の鎖長延長剤を用いて形成されてもよい。
ポリアミド系熱可塑性エラストマーとしては、具体的には、JIS K6418:2007に規定されるアミド系熱可塑性エラストマー(TPA)等や、特開2004-346273号公報に記載のポリアミド系エラストマー等を挙げることができる。
ポリアミド系熱可塑性エラストマーとは、結晶性で融点の高いハードセグメントを形成するポリマーと、非晶性でガラス転移温度の低いソフトセグメントを形成するポリマーと、を有する共重合体からなる熱可塑性の樹脂材料であって、前記ハードセグメントを形成するポリマーの主鎖にアミド結合(-CONH-)を有するものを意味する。
ポリアミド系熱可塑性エラストマーとしては、例えば、少なくともポリアミドが結晶性で融点の高いハードセグメントを形成し、他のポリマー(例えば、ポリエステル、又はポリエーテル等)が非晶性でガラス転移温度の低いソフトセグメントを形成している材料が挙げられる。また、ポリアミド系熱可塑性エラストマーは、ハードセグメント及びソフトセグメントの他に、ジカルボン酸等の鎖長延長剤を用いて形成されてもよい。
ポリアミド系熱可塑性エラストマーとしては、具体的には、JIS K6418:2007に規定されるアミド系熱可塑性エラストマー(TPA)等や、特開2004-346273号公報に記載のポリアミド系エラストマー等を挙げることができる。
ポリアミド系熱可塑性エラストマーにおいて、ハードセグメントを形成するポリアミドとしては、例えば、下記一般式(1)又は一般式(2)で表されるモノマーによって生成されるポリアミドを挙げることができる。

一般式(1)
[一般式(1)中、R1は、炭素数2~20の炭化水素の分子鎖(例えば炭素数2~20のアルキレン基)を表す。]
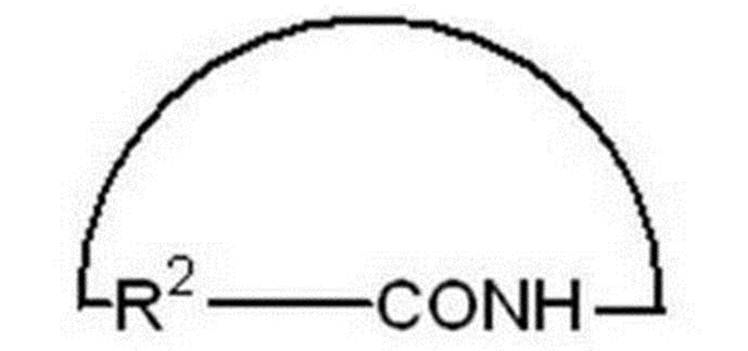
一般式(2)
[一般式(2)中、R2は、炭素数3~20の炭化水素の分子鎖(例えば炭素数3~20のアルキレン基)を表す。]
一般式(1)中、R1としては、炭素数3~18の炭化水素の分子鎖(例えば炭素数3~18のアルキレン基)が好ましく、炭素数4~15の炭化水素の分子鎖(例えば炭素数4~15のアルキレン基)が更に好ましく、炭素数10~15の炭化水素の分子鎖(例えば炭素数10~15のアルキレン基)が特に好ましい。
また、一般式(2)中、R2としては、炭素数3~18の炭化水素の分子鎖(例えば炭素数3~18のアルキレン基)が好ましく、炭素数4~15の炭化水素の分子鎖(例えば炭素数4~15のアルキレン基)が更に好ましく、炭素数10~15の炭化水素の分子鎖(例えば炭素数10~15のアルキレン基)が特に好ましい。
一般式(1)又は一般式(2)で表されるモノマーとしては、ω-アミノカルボン酸又はラクタムが挙げられる。また、ハードセグメントを形成するポリアミドとしては、これらω-アミノカルボン酸又はラクタムの重縮合体、及びジアミンとジカルボン酸との共縮重合体等が挙げられる。
また、一般式(2)中、R2としては、炭素数3~18の炭化水素の分子鎖(例えば炭素数3~18のアルキレン基)が好ましく、炭素数4~15の炭化水素の分子鎖(例えば炭素数4~15のアルキレン基)が更に好ましく、炭素数10~15の炭化水素の分子鎖(例えば炭素数10~15のアルキレン基)が特に好ましい。
一般式(1)又は一般式(2)で表されるモノマーとしては、ω-アミノカルボン酸又はラクタムが挙げられる。また、ハードセグメントを形成するポリアミドとしては、これらω-アミノカルボン酸又はラクタムの重縮合体、及びジアミンとジカルボン酸との共縮重合体等が挙げられる。
ω-アミノカルボン酸としては、6-アミノカプロン酸、7-アミノヘプタン酸、8-アミノオクタン酸、10-アミノカプリン酸、11-アミノウンデカン酸、及び12-アミノドデカン酸等の炭素数5~20の脂肪族ω-アミノカルボン酸等を挙げることができる。また、ラクタムとしては、ラウリルラクタム、ε-カプロラクタム、ウデカンラクタム、ω-エナントラクタム、及び2-ピロリドン等の炭素数5~20の脂肪族ラクタム等を挙げることができる。
ジアミンとしては、例えば、エチレンジアミン、トリメチレンジアミン、テトラメチレンジアミン、ヘキサメチレンジアミン、ヘプタメチレンジアミン、オクタメチレンジアミン、ノナメチレンジアミン、デカメチレンジアミン、ウンデカメチレンジアミン、ドデカメチレンジアミン、2,2,4-トリメチルヘキサメチレンジアミン、2,4,4-トリメチルヘキサメチレンジアミン、3-メチルペンタメチレンジアミン、及びメタキシレンジアミン等の炭素数2~20の脂肪族ジアミン等のジアミン化合物を挙げることができる。
また、ジカルボン酸は、HOOC-(R3)m-COOH(R3:炭素数3~20の炭化水素の分子鎖、m:0又は1)で表すことができ、例えば、シュウ酸、コハク酸、グルタル酸、アジピン酸、ピメリン酸、スベリン酸、アゼライン酸、セバシン酸、及びドデカン二酸等の炭素数2~20の脂肪族ジカルボン酸を挙げることができる。
ハードセグメントを形成するポリアミドとしては、ラウリルラクタム、ε-カプロラクタム、又はウデカンラクタムを開環重縮合したポリアミドを好ましく用いることができる。
ジアミンとしては、例えば、エチレンジアミン、トリメチレンジアミン、テトラメチレンジアミン、ヘキサメチレンジアミン、ヘプタメチレンジアミン、オクタメチレンジアミン、ノナメチレンジアミン、デカメチレンジアミン、ウンデカメチレンジアミン、ドデカメチレンジアミン、2,2,4-トリメチルヘキサメチレンジアミン、2,4,4-トリメチルヘキサメチレンジアミン、3-メチルペンタメチレンジアミン、及びメタキシレンジアミン等の炭素数2~20の脂肪族ジアミン等のジアミン化合物を挙げることができる。
また、ジカルボン酸は、HOOC-(R3)m-COOH(R3:炭素数3~20の炭化水素の分子鎖、m:0又は1)で表すことができ、例えば、シュウ酸、コハク酸、グルタル酸、アジピン酸、ピメリン酸、スベリン酸、アゼライン酸、セバシン酸、及びドデカン二酸等の炭素数2~20の脂肪族ジカルボン酸を挙げることができる。
ハードセグメントを形成するポリアミドとしては、ラウリルラクタム、ε-カプロラクタム、又はウデカンラクタムを開環重縮合したポリアミドを好ましく用いることができる。
また、ソフトセグメントを形成するポリマーとしては、例えば、ポリエステル、及びポリエーテル等が挙げられる。具体的には、ポリエチレングリコール、ポリプロピレングリコール、ポリテトラメチレンエーテルグリコール、及びABA型トリブロックポリエーテル等が挙げられる。これらは単独で、又は2種以上を組み合わせて用いることができる。また、ポリエーテルの末端にアンモニア等を反応させることによって得られるポリエーテルジアミン等も用いることができる。
ここで、「ABA型トリブロックポリエーテル」とは、下記一般式(3)に示されるポリエーテルを意味する。
ここで、「ABA型トリブロックポリエーテル」とは、下記一般式(3)に示されるポリエーテルを意味する。
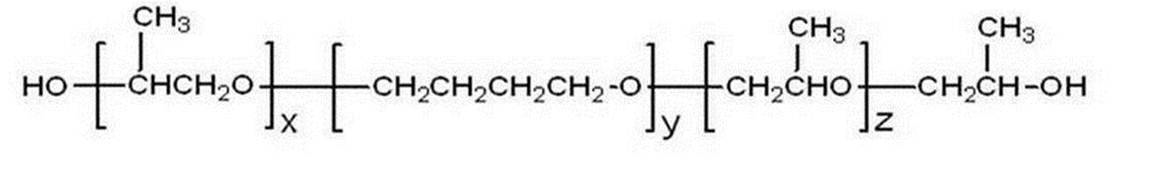
一般式(3)
[一般式(3)中、x及びzは、1~20の整数を表す。yは、4~50の整数を表す。]
一般式(3)において、x及びzは、それぞれ、1~18の整数が好ましく、1~16の整数がより好ましく、1~14の整数が更に好ましく、1~12の整数が特に好ましい。また、一般式(3)において、yは、5~45の整数が好ましく、6~40の整数がより好ましく、7~35の整数が更に好ましく、8~30の整数が特に好ましい。
ハードセグメントとソフトセグメントとの組合せとしては、上述で挙げたハードセグメントとソフトセグメントとのそれぞれの組合せを挙げることができる。これらの中でも、ハードセグメントとソフトセグメントとの組合せとしては、ラウリルラクタムの開環重縮合体とポリエチレングリコールとの組合せ、ラウリルラクタムの開環重縮合体とポリプロピレングリコールとの組合せ、ラウリルラクタムの開環重縮合体とポリテトラメチレンエーテルグリコールとの組合せ、又はラウリルラクタムの開環重縮合体とABA型トリブロックポリエーテルとの組合せが好ましく、ラウリルラクタムの開環重縮合体とABA型トリブロックポリエーテルとの組合せがより好ましい。
ハードセグメントを形成するポリマー(つまりポリアミド)の数平均分子量は、溶融成形性の観点から、300~15000が好ましい。また、ソフトセグメントを形成するポリマーの数平均分子量としては、強靱性及び低温柔軟性の観点から、200~6000が好ましい。さらに、ハードセグメント(x)及びソフトセグメント(y)の質量比(x:y)は、タイヤ骨格体の成形性の観点から、50:50~90:10が好ましく、50:50~80:20がより好ましい。
ポリアミド系熱可塑性エラストマーは、ハードセグメントを形成するポリマー及びソフトセグメントを形成するポリマーを公知の方法によって共重合することで合成することができる。
ポリアミド系熱可塑性エラストマーの市販品としては、例えば、宇部興産(株)の「UBESTA XPA」シリーズ(例えば、XPA9063X1、XPA9055X1、XPA9048X2、XPA9048X1、XPA9040X1、及びXPA9040X2XPA9044等)、ダイセル・エポニック(株)の「ベスタミド」シリーズ(例えば、E40-S3、E47-S1、E47-S3、E55-S1、E55-S3、EX9200、及びE50-R2等)等を用いることができる。
-ポリスチレン系熱可塑性エラストマー
ポリスチレン系熱可塑性エラストマーとしては、例えば、少なくともポリスチレンがハードセグメントを形成し、他のポリマー(例えば、ポリブタジエン、ポリイソプレン、ポリエチレン、水添ポリブタジエン、又は水添ポリイソプレン等)が非晶性でガラス転移温度の低いソフトセグメントを形成している材料が挙げられる。ハードセグメントを形成するポリスチレンとしては、例えば、公知のラジカル重合法、又はイオン性重合法等で得られるものが好ましく用いられ、具体的には、アニオンリビング重合を持つポリスチレンが挙げられる。また、ソフトセグメントを形成するポリマーとしては、例えば、ポリブタジエン、ポリイソプレン、及びポリ(2,3-ジメチル-ブタジエン)等が挙げられる。
ポリスチレン系熱可塑性エラストマーとしては、例えば、少なくともポリスチレンがハードセグメントを形成し、他のポリマー(例えば、ポリブタジエン、ポリイソプレン、ポリエチレン、水添ポリブタジエン、又は水添ポリイソプレン等)が非晶性でガラス転移温度の低いソフトセグメントを形成している材料が挙げられる。ハードセグメントを形成するポリスチレンとしては、例えば、公知のラジカル重合法、又はイオン性重合法等で得られるものが好ましく用いられ、具体的には、アニオンリビング重合を持つポリスチレンが挙げられる。また、ソフトセグメントを形成するポリマーとしては、例えば、ポリブタジエン、ポリイソプレン、及びポリ(2,3-ジメチル-ブタジエン)等が挙げられる。
ハードセグメントとソフトセグメントとの組合せとしては、上述で挙げたハードセグメントとソフトセグメントとのそれぞれの組合せを挙げることができる。これらの中でも、ハードセグメントとソフトセグメントとの組合せとしては、ポリスチレンとポリブタジエンとの組合せ、又はポリスチレンとポリイソプレンとの組合せが好ましい。また、熱可塑性エラストマーの意図しない架橋反応を抑制するため、ソフトセグメントは水素添加されていることが好ましい。
ハードセグメントを形成するポリマー(つまりポリスチレン)の数平均分子量は、5000~500000が好ましく、10000~200000がより好ましい。
また、ソフトセグメントを形成するポリマーの数平均分子量としては、5000~1000000が好ましく、10000~800000がより好ましく、30000~500000が更に好ましい。さらに、ハードセグメント(x)及びソフトセグメント(y)の体積比(x:y)は、タイヤ骨格体の成形性の観点から、5:95~80:20が好ましく、10:90~70:30がより好ましい。
また、ソフトセグメントを形成するポリマーの数平均分子量としては、5000~1000000が好ましく、10000~800000がより好ましく、30000~500000が更に好ましい。さらに、ハードセグメント(x)及びソフトセグメント(y)の体積比(x:y)は、タイヤ骨格体の成形性の観点から、5:95~80:20が好ましく、10:90~70:30がより好ましい。
ポリスチレン系熱可塑性エラストマーは、ハードセグメントを形成するポリマー及びソフトセグメントを形成するポリマーを公知の方法によって共重合することで合成することができる。
ポリスチレン系熱可塑性エラストマーとしては、例えば、スチレン-ブタジエン系共重合体[例えばSBS(ポリスチレン-ポリ(ブチレン)ブロック-ポリスチレン)、及びSEBS(ポリスチレン-ポリ(エチレン/ブチレン)ブロック-ポリスチレン)]、スチレン-イソプレン共重合体(例えばポリスチレン-ポリイソプレンブロック-ポリスチレン)、スチレン-プロピレン系共重合体[例えばSEP(ポリスチレン-(エチレン/プロピレン)ブロック)、SEPS(ポリスチレン-ポリ(エチレン/プロピレン)ブロック-ポリスチレン)、SEEPS(ポリスチレン-ポリ(エチレン-エチレン/プロピレン)ブロック-ポリスチレン)、及びSEB(ポリスチレン(エチレン/ブチレン)ブロック)]等が挙げられる。
ポリスチレン系熱可塑性エラストマーとしては、例えば、スチレン-ブタジエン系共重合体[例えばSBS(ポリスチレン-ポリ(ブチレン)ブロック-ポリスチレン)、及びSEBS(ポリスチレン-ポリ(エチレン/ブチレン)ブロック-ポリスチレン)]、スチレン-イソプレン共重合体(例えばポリスチレン-ポリイソプレンブロック-ポリスチレン)、スチレン-プロピレン系共重合体[例えばSEP(ポリスチレン-(エチレン/プロピレン)ブロック)、SEPS(ポリスチレン-ポリ(エチレン/プロピレン)ブロック-ポリスチレン)、SEEPS(ポリスチレン-ポリ(エチレン-エチレン/プロピレン)ブロック-ポリスチレン)、及びSEB(ポリスチレン(エチレン/ブチレン)ブロック)]等が挙げられる。
ポリスチレン系熱可塑性エラストマーの市販品としては、例えば、旭化成(株)製の「タフテック」シリーズ(例えば、H1031、H1041、H1043、H1051、H1052、H1053、H1062、H1082、H1141、H1221、及びH1272等)、(株)クラレ製の「SEBS」シリーズ(8007、及び8076等)、「SEPS」シリーズ(2002、及び2063等)等を用いることができる。
-ポリウレタン系熱可塑性エラストマー-
ポリウレタン系熱可塑性エラストマーとしては、例えば、少なくともポリウレタンが物理的な凝集によって疑似架橋を形成しているハードセグメントを形成し、他のポリマーが非晶性でガラス転移温度の低いソフトセグメントを形成している材料が挙げられる。
ポリウレタン系熱可塑性エラストマーとしては、具体的には、JIS K6418:2007に規定されるポリウレタン系熱可塑性エラストマー(TPU)が挙げられる。ポリウレタン系熱可塑性エラストマーは、下記式Aで表される単位構造を含むソフトセグメントと、下記式Bで表される単位構造を含むハードセグメントと、を含む共重合体として表すことができる。
ポリウレタン系熱可塑性エラストマーとしては、例えば、少なくともポリウレタンが物理的な凝集によって疑似架橋を形成しているハードセグメントを形成し、他のポリマーが非晶性でガラス転移温度の低いソフトセグメントを形成している材料が挙げられる。
ポリウレタン系熱可塑性エラストマーとしては、具体的には、JIS K6418:2007に規定されるポリウレタン系熱可塑性エラストマー(TPU)が挙げられる。ポリウレタン系熱可塑性エラストマーは、下記式Aで表される単位構造を含むソフトセグメントと、下記式Bで表される単位構造を含むハードセグメントと、を含む共重合体として表すことができる。
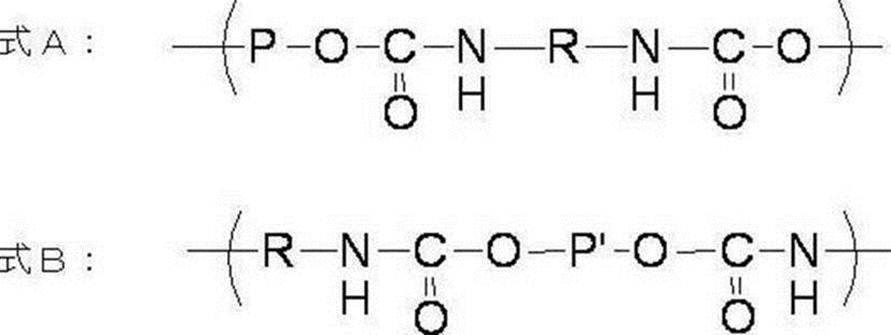
[式中、Pは、長鎖脂肪族ポリエーテル又は長鎖脂肪族ポリエステルを表す。Rは、脂肪族炭化水素、脂環族炭化水素、又は芳香族炭化水素を表す。P’は、短鎖脂肪族炭化水素、脂環族炭化水素、又は芳香族炭化水素を表す。]
式A中、Pで表される長鎖脂肪族ポリエーテル又は長鎖脂肪族ポリエステルとしては、例えば、分子量500~5000のものを使用することができる。Pは、Pで表される長鎖脂肪族ポリエーテル又は長鎖脂肪族ポリエステルを含むジオール化合物に由来する。このようなジオール化合物としては、例えば、分子量が前記範囲内にある、ポリエチレングリコール、ポリプロピレングリコール、ポリテトラメチレンエーテルグリコール、ポリ(ブチレンアジベート)ジオール、ポリ-ε-カプロラクトンジオール、ポリ(ヘキサメチレンカーボネート)ジオール、及びABA型トリブロックポリエーテル等が挙げられる。
これらは、単独で、又は2種以上を組み合わせて用いることができる。
これらは、単独で、又は2種以上を組み合わせて用いることができる。
式A及び式B中、Rは、Rで表される脂肪族炭化水素、脂環族炭化水素、又は芳香族炭化水素を含むジイソシアネート化合物に由来する。Rで表される脂肪族炭化水素を含む脂肪族ジイソシアネート化合物としては、例えば、1,2-エチレンジイソシアネート、1,3-プロピレンジイソシアネート、1,4-ブタンジイソシアネート、及び1,6-ヘキサメチレンジイソシアネート等が挙げられる。
また、Rで表される脂環族炭化水素を含むジイソシアネート化合物としては、例えば、1,4-シクロヘキサンジイソシアネート、及び4,4-シクロヘキサンジイソシアネート等が挙げられる。さらに、Rで表される芳香族炭化水素を含む芳香族ジイソシアネート化合物としては、例えば、4,4’-ジフェニルメタンジイソシアネート、及びトリレンジイソシアネート等が挙げられる。
これらは、単独で、又は2種以上を組み合わせて用いることができる。
また、Rで表される脂環族炭化水素を含むジイソシアネート化合物としては、例えば、1,4-シクロヘキサンジイソシアネート、及び4,4-シクロヘキサンジイソシアネート等が挙げられる。さらに、Rで表される芳香族炭化水素を含む芳香族ジイソシアネート化合物としては、例えば、4,4’-ジフェニルメタンジイソシアネート、及びトリレンジイソシアネート等が挙げられる。
これらは、単独で、又は2種以上を組み合わせて用いることができる。
式B中、P’で表される短鎖脂肪族炭化水素、脂環族炭化水素、又は芳香族炭化水素としては、例えば、分子量500未満のものを使用することができる。また、P’は、P’で表される短鎖脂肪族炭化水素、脂環族炭化水素、又は芳香族炭化水素を含むジオール化合物に由来する。P’で表される短鎖脂肪族炭化水素を含む脂肪族ジオール化合物としては、例えば、グリコール及びポリアルキレングリコールが挙げられ、具体的には、エチレングリコール、プロピレングリコール、トリメチレングリコール、1,4-ブタンジオール、1,3-ブタンジオール、1,5-ペンタンジオール、1,6-ヘキサンジオール、1,7-ヘプタンジオール、1,8-オクタンジオール、1,9-ノナンジオール、及び1,10-デカンジオール等が挙げられる。
また、P’で表される脂環族炭化水素を含む脂環族ジオール化合物としては、例えば、シクロペンタン-1,2-ジオール、シクロヘキサン-1,2-ジオール、シクロヘキサン-1,3-ジオール、シクロヘキサン-1,4-ジオール、及びシクロヘキサン-1,4-ジメタノール等が挙げられる。
さらに、P’で表される芳香族炭化水素を含む芳香族ジオール化合物としては、例えば、ヒドロキノン、レゾルシン、クロロヒドロキノン、ブロモヒドロキノン、メチルヒドロキノン、フェニルヒドロキノン、メトキシヒドロキノン、フェノキシヒドロキノン、4,4’-ジヒドロキシビフェニル、4,4’-ジヒドロキシジフェニルエーテル、4,4’-ジヒドロキシジフェニルサルファイド、4,4’-ジヒドロキシジフェニルスルホン、4,4’-ジヒドロキシベンゾフェノン、4,4’-ジヒドロキシジフェニルメタン、ビスフェノールA、1,1-ジ(4-ヒドロキシフェニル)シクロヘキサン、1,2-ビス(4-ヒドロキシフェノキシ)エタン、1,4-ジヒドロキシナフタリン、及び2,6-ジヒドロキシナフタリン等が挙げられる。
これらは、単独で、又は2種以上を組み合わせて用いることができる。
また、P’で表される脂環族炭化水素を含む脂環族ジオール化合物としては、例えば、シクロペンタン-1,2-ジオール、シクロヘキサン-1,2-ジオール、シクロヘキサン-1,3-ジオール、シクロヘキサン-1,4-ジオール、及びシクロヘキサン-1,4-ジメタノール等が挙げられる。
さらに、P’で表される芳香族炭化水素を含む芳香族ジオール化合物としては、例えば、ヒドロキノン、レゾルシン、クロロヒドロキノン、ブロモヒドロキノン、メチルヒドロキノン、フェニルヒドロキノン、メトキシヒドロキノン、フェノキシヒドロキノン、4,4’-ジヒドロキシビフェニル、4,4’-ジヒドロキシジフェニルエーテル、4,4’-ジヒドロキシジフェニルサルファイド、4,4’-ジヒドロキシジフェニルスルホン、4,4’-ジヒドロキシベンゾフェノン、4,4’-ジヒドロキシジフェニルメタン、ビスフェノールA、1,1-ジ(4-ヒドロキシフェニル)シクロヘキサン、1,2-ビス(4-ヒドロキシフェノキシ)エタン、1,4-ジヒドロキシナフタリン、及び2,6-ジヒドロキシナフタリン等が挙げられる。
これらは、単独で、又は2種以上を組み合わせて用いることができる。
ハードセグメントを形成するポリマー(つまりポリウレタン)の数平均分子量は、溶融成形性の観点から、300~1500が好ましい。また、ソフトセグメントを形成するポリマーの数平均分子量としては、ポリウレタン系熱可塑性エラストマーの柔軟性及び熱安定性の観点から、500~20000が好ましく、500~5000が更に好ましく、500~3000が特に好ましい。また、ハードセグメント(x)及びソフトセグメント(y)の質量比(x:y)は、タイヤ骨格体の成形性の観点から、15:85~90:10が好ましく、30:70~90:10が更に好ましい。
ポリウレタン系熱可塑性エラストマーは、ハードセグメントを形成するポリマー及びソフトセグメントを形成するポリマーを公知の方法によって共重合することで合成することができる。ポリウレタン系熱可塑性エラストマーとしては、例えば、特開平5-331256号公報に記載の熱可塑性ポリウレタンを用いることができる。
ポリウレタン系熱可塑性エラストマーとしては、具体的には、芳香族ジオールと芳香族ジイソシアネートとのみからなるハードセグメントと、ポリ炭酸エステルのみからなるソフトセグメントとの組合せが好ましく、より具体的には、トリレンジイソシアネート(TDI)/ポリエステル系ポリオール共重合体、TDI/ポリエーテル系ポリオール共重合体、TDI/カプロラクトン系ポリオール共重合体、TDI/ポリカーボネート系ポリオール共重合体、4,4’-ジフェニルメタンジイソシアネート(MDI)/ポリエステル系ポリオール共重合体、MDI/ポリエーテル系ポリオール共重合体、MDI/カプロラクトン系ポリオール共重合体、MDI/ポリカーボネート系ポリオール共重合体、及びMDI+ヒドロキノン/ポリヘキサメチレンカーボネート共重合体から選ばれる少なくとも1種が好ましい。中でも、TDI/ポリエステル系ポリオール共重合体、TDI/ポリエーテル系ポリオール共重合体、MDI/ポリエステルポリオール共重合体、MDI/ポリエーテル系ポリオール共重合体、及びMDI+ヒドロキノン/ポリヘキサメチレンカーボネート共重合体から選ばれる少なくとも1種が更に好ましい。
ポリウレタン系熱可塑性エラストマーとしては、具体的には、芳香族ジオールと芳香族ジイソシアネートとのみからなるハードセグメントと、ポリ炭酸エステルのみからなるソフトセグメントとの組合せが好ましく、より具体的には、トリレンジイソシアネート(TDI)/ポリエステル系ポリオール共重合体、TDI/ポリエーテル系ポリオール共重合体、TDI/カプロラクトン系ポリオール共重合体、TDI/ポリカーボネート系ポリオール共重合体、4,4’-ジフェニルメタンジイソシアネート(MDI)/ポリエステル系ポリオール共重合体、MDI/ポリエーテル系ポリオール共重合体、MDI/カプロラクトン系ポリオール共重合体、MDI/ポリカーボネート系ポリオール共重合体、及びMDI+ヒドロキノン/ポリヘキサメチレンカーボネート共重合体から選ばれる少なくとも1種が好ましい。中でも、TDI/ポリエステル系ポリオール共重合体、TDI/ポリエーテル系ポリオール共重合体、MDI/ポリエステルポリオール共重合体、MDI/ポリエーテル系ポリオール共重合体、及びMDI+ヒドロキノン/ポリヘキサメチレンカーボネート共重合体から選ばれる少なくとも1種が更に好ましい。
また、ポリウレタン系熱可塑性エラストマーの市販品としては、例えば、BASF社製の「エラストラン」シリーズ(例えば、ET680、ET880、ET690、及びET890等)、(株)クラレ社製の「クラミロンU」シリーズ(例えば、2000番台、3000番台、8000番台、及び9000番台等)、日本ミラクトラン(株)製の「ミラクトラン」シリーズ(例えば、XN-2001、XN-2004、P390RSUP、P480RSUI、P26MRNAT、E490、E590、及びP890等)等を用いることができる。
-オレフィン系熱可塑性エラストマー-
オレフィン系熱可塑性エラストマーとしては、例えば、少なくともポリオレフィンが結晶性で融点の高いハードセグメントを形成し、他のポリマー(例えば、他のポリオレフィン、及びポリビニル化合物等)が非晶性でガラス転移温度の低いソフトセグメントを形成している材料が挙げられる。ハードセグメントを形成するポリオレフィンとしては、例えば、ポリエチレン、ポリプロピレン、アイソタクチックポリプロピレン、及びポリブテン等が挙げられる。
オレフィン系熱可塑性エラストマーとしては、例えば、オレフィン-α-オレフィンランダム共重合体、及びオレフィンブロック共重合体等が挙げられる。具体的には、プロピレンブロック共重合体、エチレン-プロピレン共重合体、プロピレン-1-ヘキセン共重合体、プロピレン-4-メチル-1ペンテン共重合体、プロピレン-1-ブテン共重合体、エチレン-1-ヘキセン共重合体、エチレン-4-メチル-ペンテン共重合体、エチレン-1-ブテン共重合体、1-ブテン-1-ヘキセン共重合体、1-ブテン-4-メチル-ペンテン、エチレン-メタクリル酸共重合体、エチレン-メタクリル酸メチル共重合体、エチレン-メタクリル酸エチル共重合体、エチレン-メタクリル酸ブチル共重合体、エチレン-メチルアクリレート共重合体、エチレン-エチルアクリレート共重合体、エチレン-ブチルアクリレート共重合体、プロピレン-メタクリル酸共重合体、プロピレン-メタクリル酸メチル共重合体、プロピレン-メタクリル酸エチル共重合体、プロピレン-メタクリル酸ブチル共重合体、プロピレン-メチルアクリレート共重合体、プロピレン-エチルアクリレート共重合体、プロピレン-ブチルアクリレート共重合体、エチレン-酢酸ビニル共重合体、及びプロピレン-酢酸ビニル共重合体等が挙げられる。
オレフィン系熱可塑性エラストマーとしては、例えば、少なくともポリオレフィンが結晶性で融点の高いハードセグメントを形成し、他のポリマー(例えば、他のポリオレフィン、及びポリビニル化合物等)が非晶性でガラス転移温度の低いソフトセグメントを形成している材料が挙げられる。ハードセグメントを形成するポリオレフィンとしては、例えば、ポリエチレン、ポリプロピレン、アイソタクチックポリプロピレン、及びポリブテン等が挙げられる。
オレフィン系熱可塑性エラストマーとしては、例えば、オレフィン-α-オレフィンランダム共重合体、及びオレフィンブロック共重合体等が挙げられる。具体的には、プロピレンブロック共重合体、エチレン-プロピレン共重合体、プロピレン-1-ヘキセン共重合体、プロピレン-4-メチル-1ペンテン共重合体、プロピレン-1-ブテン共重合体、エチレン-1-ヘキセン共重合体、エチレン-4-メチル-ペンテン共重合体、エチレン-1-ブテン共重合体、1-ブテン-1-ヘキセン共重合体、1-ブテン-4-メチル-ペンテン、エチレン-メタクリル酸共重合体、エチレン-メタクリル酸メチル共重合体、エチレン-メタクリル酸エチル共重合体、エチレン-メタクリル酸ブチル共重合体、エチレン-メチルアクリレート共重合体、エチレン-エチルアクリレート共重合体、エチレン-ブチルアクリレート共重合体、プロピレン-メタクリル酸共重合体、プロピレン-メタクリル酸メチル共重合体、プロピレン-メタクリル酸エチル共重合体、プロピレン-メタクリル酸ブチル共重合体、プロピレン-メチルアクリレート共重合体、プロピレン-エチルアクリレート共重合体、プロピレン-ブチルアクリレート共重合体、エチレン-酢酸ビニル共重合体、及びプロピレン-酢酸ビニル共重合体等が挙げられる。
これらの中でも、オレフィン系熱可塑性エラストマーとしては、プロピレンブロック共重合体、エチレン-プロピレン共重合体、プロピレン-1-ヘキセン共重合体、プロピレン-4-メチル-1ペンテン共重合体、プロピレン-1-ブテン共重合体、エチレン-1-ヘキセン共重合体、エチレン-4-メチル-ペンテン共重合体、エチレン-1-ブテン共重合体、エチレン-メタクリル酸共重合体、エチレン-メタクリル酸メチル共重合体、エチレン-メタクリル酸エチル共重合体、エチレン-メタクリル酸ブチル共重合体、エチレン-メチルアクリレート共重合体、エチレン-エチルアクリレート共重合体、エチレン-ブチルアクリレート共重合体、プロピレン-メタクリル酸共重合体、プロピレン-メタクリル酸メチル共重合体、プロピレン-メタクリル酸エチル共重合体、プロピレン-メタクリル酸ブチル共重合体、プロピレン-メチルアクリレート共重合体、プロピレン-エチルアクリレート共重合体、プロピレン-ブチルアクリレート共重合体、エチレン-酢酸ビニル共重合体、及びプロピレン-酢酸ビニル共重合体から選ばれる少なくとも1種が好ましく、エチレン-プロピレン共重合体、プロピレン-1-ブテン共重合体、エチレン-1-ブテン共重合体、エチレン-メタクリル酸メチル共重合体、エチレン-メチルアクリレート共重合体、エチレン-エチルアクリレート共重合体、及びエチレン-ブチルアクリレート共重合体から選ばれる少なくとも1種が更に好ましい。
また、エチレンとプロピレンといったように、2種以上のオレフィン樹脂を組み合わせて用いてもよい。また、オレフィン系熱可塑性エラストマー中のオレフィン樹脂含有率は、50質量%以上100質量%以下が好ましい。
また、エチレンとプロピレンといったように、2種以上のオレフィン樹脂を組み合わせて用いてもよい。また、オレフィン系熱可塑性エラストマー中のオレフィン樹脂含有率は、50質量%以上100質量%以下が好ましい。
オレフィン系熱可塑性エラストマーの数平均分子量は、5000~10000000であることが好ましい。オレフィン系熱可塑性エラストマーの数平均分子量が5000~10000000であると、熱可塑性樹脂材料の機械的物性が十分であり、加工性にも優れる。同様の観点から、オレフィン系熱可塑性エラストマーの数平均分子量は、7000~1000000であることが更に好ましく、10000~1000000が特に好ましい。これにより、熱可塑性樹脂材料の機械的物性及び加工性を更に向上させることができる。また、ソフトセグメントを形成するポリマーの数平均分子量としては、強靱性及び低温柔軟性の観点から、200~6000が好ましい。更に、ハードセグメント(x)及びソフトセグメント(y)の質量比(x:y)は、タイヤ骨格体の成形性の観点から、50:50~95:15が好ましく、50:50~90:10が更に好ましい。
オレフィン系熱可塑性エラストマーは、公知の方法によって共重合することで合成することができる。
オレフィン系熱可塑性エラストマーは、公知の方法によって共重合することで合成することができる。
また、オレフィン系熱可塑性エラストマーとしては、オレフィン系熱可塑性エラストマーを酸変性してなるものを用いてもよい。
「オレフィン系熱可塑性エラストマーを酸変性してなるもの」とは、オレフィン系熱可塑性エラストマーに、カルボン酸基、硫酸基、及び燐酸基等の酸性基を有する不飽和化合物を結合させることをいう。
オレフィン熱可塑性エラストマーに、カルボン酸基、硫酸基、及び燐酸基等の酸性基を有する不飽和化合物を結合させることとしては、例えば、オレフィン系熱可塑性エラストマーに、酸性基を有する不飽和化合物として、不飽和カルボン酸(例えば、一般的には、無水マレイン酸)の不飽和結合部位を結合(例えば、グラフト重合)させることが挙げられる。
酸性基を有する不飽和化合物としては、オレフィン系熱可塑性エラストマーの劣化抑制の観点からは、弱酸基であるカルボン酸基を有する不飽和化合物が好ましく、例えば、アクリル酸、メタクリル酸、イタコン酸、クロトン酸、イソクロトン酸、及びマレイン酸等が挙げられる。
「オレフィン系熱可塑性エラストマーを酸変性してなるもの」とは、オレフィン系熱可塑性エラストマーに、カルボン酸基、硫酸基、及び燐酸基等の酸性基を有する不飽和化合物を結合させることをいう。
オレフィン熱可塑性エラストマーに、カルボン酸基、硫酸基、及び燐酸基等の酸性基を有する不飽和化合物を結合させることとしては、例えば、オレフィン系熱可塑性エラストマーに、酸性基を有する不飽和化合物として、不飽和カルボン酸(例えば、一般的には、無水マレイン酸)の不飽和結合部位を結合(例えば、グラフト重合)させることが挙げられる。
酸性基を有する不飽和化合物としては、オレフィン系熱可塑性エラストマーの劣化抑制の観点からは、弱酸基であるカルボン酸基を有する不飽和化合物が好ましく、例えば、アクリル酸、メタクリル酸、イタコン酸、クロトン酸、イソクロトン酸、及びマレイン酸等が挙げられる。
オレフィン系熱可塑性エラストマーの市販品としては、例えば、三井化学(株)製の「タフマー」シリーズ(例えば、A0550S、A1050S、A4050S、A1070S、A4070S、A35070S、A1085S、A4085S、A7090、A70090、MH7007、MH7010、XM-7070、XM-7080、BL4000、BL2481、BL3110、BL3450、P-0275、P-0375、P-0775、P-0180、P-0280、P-0480、及びP-0680等)、三井・デュポンポリケミカル(株)製の「ニュクレル」シリーズ(例えば、AN4214C、AN4225C、AN42115C、N0903HC、N0908C、AN42012C、N410、N1050H、N1108C、N1110H、N1207C、N1214、AN4221C、N1525、N1560、N0200H、AN4228C、AN4213C、及びN035C)等、「エルバロイAC」シリーズ(例えば、1125AC、1209AC、1218AC、1609AC、1820AC、1913AC、2112AC、2116AC、2615AC、2715AC、3117AC、3427AC、及び3717AC等)、住友化学(株)の「アクリフト」シリーズ、及び「エバテート」シリーズ等、東ソー(株)製の「ウルトラセン」シリーズ等、プライムポリマー製の「プライムTPO」シリーズ(例えば、E-2900H、F-3900H、E-2900、F-3900、J-5900、E-2910、F-3910、J-5910、E-2710、F-3710、J-5910、E-2740、F-3740、R110MP、R110E、T310E、及びM142E等)等も用いることができる。
-添加剤-
樹脂材料は、所望により、熱可塑性エラストマー以外の成分を含んでもよい。熱可塑性エラストマー以外の成分としては、ゴム、熱可塑性樹脂、充填剤(例えばシリカ、炭酸カルシウム、及びクレイ等)、老化防止剤、オイル、可塑剤、発色剤、並びに耐候剤等が挙げられる。
樹脂材料は、所望により、熱可塑性エラストマー以外の成分を含んでもよい。熱可塑性エラストマー以外の成分としては、ゴム、熱可塑性樹脂、充填剤(例えばシリカ、炭酸カルシウム、及びクレイ等)、老化防止剤、オイル、可塑剤、発色剤、並びに耐候剤等が挙げられる。
樹脂材料に可塑剤を配合すると、タイヤの転がり性能が向上し、かつ射出成型性が向上するという効果が得られることが分かっている。一方、可塑剤の配合量を多くしすぎると、ブルーム・ブリード現象の発生から、他材料との接着性に影響を及ぼす可能性がある。そこで、使用する熱可塑性エラストマーとの相溶性の高い可塑剤を選択して用いることで、ブルーム・ブリード現象を防ぎ、タイヤの転がり性能を向上しつつ、成型性及び安全性を確保することが好ましい。
樹脂材料が熱可塑性エラストマー以外の成分を含む場合、本開示の効果を十分に達成する観点からは、樹脂材料中の熱可塑性エラストマーの含有率が50質量%以上であることが好ましく、80質量%以上であることがより好ましく、90質量%以上であることが更に好ましい。
-樹脂材料の物性-
樹脂材料に含まれる熱可塑性エラストマーの結晶化温度は、148℃~160℃の範囲内であることが好ましく、150℃~155℃の範囲内であることがより好ましく、152℃~154℃の範囲内であることがさらに好ましい。結晶化温度が上記の範囲であることで、非晶部の厚みLaや、長周期L、配向度f、結晶化度Xc等を前述の範囲に制御し易くなり、その結果タイヤの耐久性、特に衝撃に対する耐亀裂性を向上させ易くなる。
なお、熱可塑性エラストマーの結晶化温度は示差走査熱量測定(DSC)により測定される。
樹脂材料が2種以上の熱可塑性エラストマーを含む場合、質量基準で最も含有率の高い熱可塑性エラストマーの結晶化温度が上記範囲内であることが好ましい。また、質量基準で最も含有率の高い熱可塑性エラストマーを含めて、結晶化温度が上記範囲内である熱可塑性エラストマーを2種以上含むことがより好ましく、含まれる全ての熱可塑性エラストマーの結晶化温度が上記範囲内であることがさらに好ましい。
樹脂材料に含まれる熱可塑性エラストマーの結晶化温度は、148℃~160℃の範囲内であることが好ましく、150℃~155℃の範囲内であることがより好ましく、152℃~154℃の範囲内であることがさらに好ましい。結晶化温度が上記の範囲であることで、非晶部の厚みLaや、長周期L、配向度f、結晶化度Xc等を前述の範囲に制御し易くなり、その結果タイヤの耐久性、特に衝撃に対する耐亀裂性を向上させ易くなる。
なお、熱可塑性エラストマーの結晶化温度は示差走査熱量測定(DSC)により測定される。
樹脂材料が2種以上の熱可塑性エラストマーを含む場合、質量基準で最も含有率の高い熱可塑性エラストマーの結晶化温度が上記範囲内であることが好ましい。また、質量基準で最も含有率の高い熱可塑性エラストマーを含めて、結晶化温度が上記範囲内である熱可塑性エラストマーを2種以上含むことがより好ましく、含まれる全ての熱可塑性エラストマーの結晶化温度が上記範囲内であることがさらに好ましい。
樹脂材料の融点は、通常100℃~350℃程度であるが、タイヤの耐久性及び生産性の観点から、100℃~250℃程度が好ましく、120℃~250℃がより好ましい。
樹脂材料(つまりタイヤ骨格体)自体のJIS K7113:1995に規定される引張弾性率は、50MPa~1000MPaが好ましく、50MPa~800MPaが更に好ましく、50MPa~700MPaが特に好ましい。樹脂材料の引張弾性率が、50MPa~1000MPaであると、タイヤ骨格体の形状を保持しつつ、リム組みを効率的に行なうことができる。
樹脂材料(つまりタイヤ骨格体)自体のJIS K7113(1995)に規定される引張強さは、通常、15MPa~70MPa程度であり、17MPa~60MPaが好ましく、20MPa~55MPaが更に好ましい。
樹脂材料(つまりタイヤ骨格体)自体のJIS K7113(1995)に規定される引張降伏強さは、5MPa以上が好ましく、5MPa~20MPaが更に好ましく、5MPa~17MPaが特に好ましい。樹脂材料の引張降伏強さが、5MPa以上であると、走行時等にタイヤにかかる荷重に対する変形に耐えることができる。
樹脂材料(つまりタイヤ骨格体)自体のJIS K7113(1995)に規定される引張降伏伸びは、10%以上が好ましく、10%~70%が更に好ましく、15%~60%が特に好ましい。樹脂材料の引張降伏伸びが、10%以上であると、弾性領域が大きく、リム組み性を良好にすることができる。
樹脂材料(つまりタイヤ骨格体)自体のJIS K7113(1995)に規定される引張破断伸びは、50%以上が好ましく、100%以上が更に好ましく、150%以上が特に好ましく、200%以上が最も好ましい。樹脂材料の引張破断伸びが、50%以上であると、リム組み性が良好であり、衝突に対して破壊し難くすることができる。
樹脂材料(つまりタイヤ骨格体)自体のISO 75-2又はASTM D648に規定される荷重たわみ温度(条件:0.45MPa荷重時)は、50℃以上が好ましく、50℃~150℃が更に好ましく、50℃~130℃が特に好ましい。樹脂材料の荷重たわみ温度が、50℃以上であると、タイヤの製造において加硫を行う場合であってもタイヤ骨格体の変形を抑制するこができる。
樹脂材料(つまりタイヤ骨格体)自体のJIS K7206(2016)に規定されるビカット軟化温度(A法)としては、130℃以上が好ましく、130~250℃が好ましく、130~220℃がさらに好ましい。熱可塑性樹脂材料の軟化温度(A法)が、130℃以上であると、使用環境におけるタイヤの軟化や変形を抑制することができる。また、タイヤの製造の際に接合において加硫を行う場合であってもタイヤ骨格体の変形を抑制することができる。
[タイヤにおけるタイヤ骨格体以外の構成]
本実施形態に係るタイヤは、必要に応じて、タイヤ骨格体以外の部材を含んでもよい。例えば、タイヤ骨格体の外周等に配置される、タイヤ骨格体を補強するための補強部材を含んでもよい。
補強部材としては、スチールコード等の金属部材を含んで形成されるコード部材が挙げられ、またコード部材を被覆樹脂材料で被覆したものも用いられる。
本実施形態に係るタイヤは、必要に応じて、タイヤ骨格体以外の部材を含んでもよい。例えば、タイヤ骨格体の外周等に配置される、タイヤ骨格体を補強するための補強部材を含んでもよい。
補強部材としては、スチールコード等の金属部材を含んで形成されるコード部材が挙げられ、またコード部材を被覆樹脂材料で被覆したものも用いられる。
補強部材中の被覆樹脂材料に用いられる樹脂としては、熱硬化性樹脂、熱可塑性樹脂、及び熱可塑性エラストマー等が挙げられる。
熱硬化性樹脂としては、例えば、フェノール樹脂、ユリア樹脂、メラミン樹脂、エポキシ樹脂、ポリアミド樹脂、及びポリエステル樹脂等が挙げられる。
熱可塑性樹脂としては、例えば、ウレタン樹脂、オレフィン樹脂、塩化ビニル樹脂、ポリアミド樹脂、及びポリエステル樹脂等が挙げられる。
熱可塑性エラストマーとしては、例えば、JIS K6418:2007に規定されるポリエステル系熱可塑性エラストマー(TPC)、ポリアミド系熱可塑性エラストマー(TPA)、ポリオレフィン系熱可塑性エラストマー(TPO)、ポリスチレン系熱可塑性エラストマー(TPS)、ポリウレタン系熱可塑性エラストマー(TPU)、熱可塑性ゴム架橋体(TPV)、又はその他の熱可塑性エラストマー(TPZ)等が挙げられる。なお、走行時に求められる弾性と製造時の成形性等を考慮すると、これらの中でも熱可塑性エラストマーを用いることが好ましい。
また、タイヤ骨格体を形成する樹脂材料中に含まれる熱可塑性エラストマーと同種の熱可塑性エラストマーを含むことが好ましい。
熱硬化性樹脂としては、例えば、フェノール樹脂、ユリア樹脂、メラミン樹脂、エポキシ樹脂、ポリアミド樹脂、及びポリエステル樹脂等が挙げられる。
熱可塑性樹脂としては、例えば、ウレタン樹脂、オレフィン樹脂、塩化ビニル樹脂、ポリアミド樹脂、及びポリエステル樹脂等が挙げられる。
熱可塑性エラストマーとしては、例えば、JIS K6418:2007に規定されるポリエステル系熱可塑性エラストマー(TPC)、ポリアミド系熱可塑性エラストマー(TPA)、ポリオレフィン系熱可塑性エラストマー(TPO)、ポリスチレン系熱可塑性エラストマー(TPS)、ポリウレタン系熱可塑性エラストマー(TPU)、熱可塑性ゴム架橋体(TPV)、又はその他の熱可塑性エラストマー(TPZ)等が挙げられる。なお、走行時に求められる弾性と製造時の成形性等を考慮すると、これらの中でも熱可塑性エラストマーを用いることが好ましい。
また、タイヤ骨格体を形成する樹脂材料中に含まれる熱可塑性エラストマーと同種の熱可塑性エラストマーを含むことが好ましい。
また、コード部材が接着剤(つまり接着層)を介して被覆樹脂材料で被覆された構造を有する補強部材を用いてもよく、この補強部材がタイヤ骨格体上に配置されていてもよい。この場合、タイヤ骨格体のマルテンス硬度(d1)、被覆樹脂材料のマルテンス硬度(d2)、及び接着層のマルテンス硬度(d3)が、d1≦d2<d3の関係を満たすことが好ましい。被覆樹脂材料のマルテンス硬度を、接着層のマルテンス硬度よりも小さくし、かつ、タイヤ骨格体のマルテンス硬度よりも大きくするか又は同等に設定することで、タイヤ骨格体を形成する樹脂材料とコード部材との剛性段差が効果的に緩和される。その結果、タイヤの耐久性を更に向上させることができる。
[タイヤの構成]
以下、図面を参照して本実施形態に係るタイヤの一実施形態について説明する。なお、同じ機能及び作用を有する部材には、全図面を通して同じ符号を付与することがあり、その場合該符号の説明を省略することがある。
図1Aは、第一実施形態に係るタイヤ10の一部の断面を示す斜視図である。図1Bは、第一実施形態に係るタイヤ10をリムに装着したときのビード部の断面図である。図1Aに示すように、タイヤ10は、従来から一般に用いられているゴム製の空気入りタイヤと略同様の断面形状を呈している。図1Aに示すように、タイヤ10は、図1Bに示すリム20のビードシート21およびリムフランジ22に接触する1対のビード部12と、ビード部12からタイヤ径方向外側に延びるサイド部14と、一方のサイド部14のタイヤ径方向外側端と他方のサイド部14のタイヤ径方向外側端とを連結するクラウン部16(つまり外周部)と、のみからなるタイヤケース17を備えている。
以下、図面を参照して本実施形態に係るタイヤの一実施形態について説明する。なお、同じ機能及び作用を有する部材には、全図面を通して同じ符号を付与することがあり、その場合該符号の説明を省略することがある。
図1Aは、第一実施形態に係るタイヤ10の一部の断面を示す斜視図である。図1Bは、第一実施形態に係るタイヤ10をリムに装着したときのビード部の断面図である。図1Aに示すように、タイヤ10は、従来から一般に用いられているゴム製の空気入りタイヤと略同様の断面形状を呈している。図1Aに示すように、タイヤ10は、図1Bに示すリム20のビードシート21およびリムフランジ22に接触する1対のビード部12と、ビード部12からタイヤ径方向外側に延びるサイド部14と、一方のサイド部14のタイヤ径方向外側端と他方のサイド部14のタイヤ径方向外側端とを連結するクラウン部16(つまり外周部)と、のみからなるタイヤケース17を備えている。
タイヤケース17は上述したタイヤ骨格体に相当し、上述した樹脂材料で形成されている。第一実施形態においてタイヤケース17は、その全体が上述した樹脂材料で形成されているが、本開示はこの構成に限定されない。従来から一般に用いられているゴム製の空気入りタイヤと同様に、タイヤケース17の各部位毎(例えばサイド部14、クラウン部16、ビード部12など)に異なる樹脂材料を用いてもよい。また、タイヤケース17の各部位を補強するために、補強材(例えば高分子材料や金属製の繊維、コード、不織布、織布等)をタイヤケース17の各部位に埋設して配置してもよい。
第一実施形態のタイヤケース17は、タイヤケース17の周方向に沿ってトレッド幅を等分した状態の形状であるタイヤケース半体(つまりタイヤ骨格片)を2つ作製し、これらをタイヤの赤道面部分で接合させることで形成される。なお、タイヤケース17は、2つの部材(つまり2つのタイヤケース半体)を接合して形成するものに限らず、3以上の部材を接合して形成してもよい。
タイヤケース半体は、例えば、真空成形、圧空成形、インジェクション成形、及びメルトキャスティング等の方法で作製できる。このため、従来のようにゴムでタイヤケースを成形する場合に比較して、加硫を行う必要がなく、製造工程を大幅に簡略化でき、成形時間を短縮することができる。
第一実施形態において、図1Bに示すビード部12には、従来から一般に用いられている空気入りタイヤと同様に、円環状のビードコア18が埋設されている。第一実施形態ではビードコア18としてスチールコードを用いるが、有機繊維コード、樹脂被覆した有機繊維コード、又は硬質樹脂コード等を用いてもよい。なお、ビード部12の剛性が確保され、リム20との嵌合が良好であれば、ビードコア18を省略することもできる。
第一実施形態では、ビード部12のリム20と接触する部分や、少なくともリム20のリムフランジ22と接触する部分には、タイヤケース17を形成する樹脂材料よりもシール性に優れた材料からなる円環状のシール層24が形成されている。シール層24は、タイヤケース17のビード部12とビードシート21とが接触する部分にも形成されていてよい。なお、タイヤケース17を形成する樹脂材料のみでリム20との間のシール性が確保できれば、シール層24は省略してもよい。タイヤケース17を形成する樹脂材料よりもシール性に優れた材料としては、タイヤケース17を形成する樹脂材料よりも軟質な材料、例えばゴム、樹脂材料よりも軟質な熱可塑性樹脂及び熱可塑性エラストマーが挙げられる。
図1Aに示すように、クラウン部16には、タイヤケース17を形成する樹脂材料よりも剛性が高い補強コード26が、タイヤケース17の周方向に巻回されている。補強コード26は、タイヤケース17の軸方向に沿った断面視で、少なくとも一部がクラウン部16に埋設された状態で螺旋状に巻回されており、補強コード層28を形成している。補強コード層28のタイヤ径方向外周側には、タイヤケース17を形成する樹脂材料よりも耐摩耗性に優れた材料、例えばゴムからなるトレッド30が配置されている。
第一実施形態では、図2に示すように、補強コード26はスチールコード等の金属部材26Aを被覆用樹脂材料27で被覆した状態(つまり被覆コード部材)である。第一実施形態では、被覆用樹脂材料27としてタイヤケース17を形成する樹脂材料と同じ樹脂材料を用いているが、他の熱可塑性樹脂又は熱可塑性エラストマーを用いてもよい。補強コード26は、クラウン部16との接触部分において、溶接、又は接着剤による接着等の方法で接合されている。なお、補強コード26は、被覆用樹脂材料27で被覆されていない状態のスチールコード等であってもよい。
被覆用樹脂材料27の弾性率は、タイヤケース17を形成する樹脂材料の弾性率の0.1倍から10倍の範囲内に設定することが好ましい。被覆用樹脂材料27の弾性率がタイヤケース17を形成する樹脂材料の弾性率の10倍以下であると、クラウン部が硬くなり過ぎず、リム組み性が容易になる。被覆用樹脂材料27の弾性率がタイヤケース17を形成する樹脂材料の弾性率の0.1倍以上であると、補強コード層28を形成する樹脂が柔らかすぎず、ベルト面内せん断剛性に優れ、コーナリング力が向上する。
第一実施形態では、図2に示すように、補強コード26は、断面形状が略台形状とされている。なお、以下では、補強コード26の上面(つまりタイヤ径方向外側の面)を符号26Uで示し、下面(つまりタイヤ径方向内側の面)を符号26Dで示す。また、第一実施形態では、補強コード26の断面形状を略台形状とする構成としているが、本開示はこの構成に限定されない。補強コード26は、断面形状が下面26D側(つまりタイヤ径方向内側)から上面26U側(つまりタイヤ径方向外側)へ向かって幅広となる形状を除いた形状であれば、いずれの形状でもよい。
図2に示すように、補強コード26は、周方向に間隔をあけて配置されていることから、隣接する補強コード26との間に隙間28Aが形成されている。このため、補強コード層28の外周面は、凹凸を有する形状となり、この補強コード層28が外周部を構成するタイヤケース17の外周面17Sも凹凸を有する形状となっている。
タイヤケース17の外周面17S(前記凹凸含む)には、微細な粗化凹凸96が形成され、その上に接合剤を介して、クッションゴム29が接合されている。クッションゴム29は、補強コード26との接触面において、粗化凹凸96を埋めるように流れ込んでいる。
クッションゴム29の上(つまりタイヤ外周面側)には、上述したトレッド30が接合されている。トレッド30には、従来のゴム製の空気入りタイヤと同様に、路面との接地面に複数の溝からなるトレッドパターン(図示省略)が形成されている。
[タイヤの製造方法]
次に、本実施形態のタイヤの製造方法について、前記第一実施形態に係るタイヤの製造方法を例にして、説明する。
(タイヤケース成形工程)
まず、タイヤケース半体を射出成形等によって成形する(成形工程)。なお、例えばこの成形工程における樹脂材料の温度、例えば射出成形の場合であればシリンダ温度や金型温度等を調整することで、タイヤケースに含まれる熱可塑性エラストマーの非晶部の厚みLa、長周期L、配向度f、及び結晶化度Xc等を前述の範囲となるよう制御することができる。
ここで、シリンダ温度としては、240℃~290℃の範囲であることが好ましく、240℃~260℃の範囲であることがより好ましく、240℃~245℃の範囲であることがさらに好ましい。
また、金型温度としては、50℃~110℃の範囲であることが好ましく、50℃~80℃の範囲であることがより好ましく、50℃~55℃の範囲であることがさらに好ましい。
なお、熱可塑性エラストマーの非晶部の厚みLa、長周期L、配向度f、及び結晶化度Xc等の制御には、成形工程における樹脂材料の冷却速度や冷却時間の調整が影響すると考えられる。そのため、冷却速度としては、140℃/秒~240℃/秒の範囲であることが好ましく、140℃/秒~230℃/秒の範囲であることがより好ましい。冷却時間(つまり金型温度にまで冷却する時間)としては、1秒~5秒の範囲であることが好ましく、1秒~1.5秒の範囲であることがより好ましい。
次に、本実施形態のタイヤの製造方法について、前記第一実施形態に係るタイヤの製造方法を例にして、説明する。
(タイヤケース成形工程)
まず、タイヤケース半体を射出成形等によって成形する(成形工程)。なお、例えばこの成形工程における樹脂材料の温度、例えば射出成形の場合であればシリンダ温度や金型温度等を調整することで、タイヤケースに含まれる熱可塑性エラストマーの非晶部の厚みLa、長周期L、配向度f、及び結晶化度Xc等を前述の範囲となるよう制御することができる。
ここで、シリンダ温度としては、240℃~290℃の範囲であることが好ましく、240℃~260℃の範囲であることがより好ましく、240℃~245℃の範囲であることがさらに好ましい。
また、金型温度としては、50℃~110℃の範囲であることが好ましく、50℃~80℃の範囲であることがより好ましく、50℃~55℃の範囲であることがさらに好ましい。
なお、熱可塑性エラストマーの非晶部の厚みLa、長周期L、配向度f、及び結晶化度Xc等の制御には、成形工程における樹脂材料の冷却速度や冷却時間の調整が影響すると考えられる。そのため、冷却速度としては、140℃/秒~240℃/秒の範囲であることが好ましく、140℃/秒~230℃/秒の範囲であることがより好ましい。冷却時間(つまり金型温度にまで冷却する時間)としては、1秒~5秒の範囲であることが好ましく、1秒~1.5秒の範囲であることがより好ましい。
次いで、成形工程で得られた円環状のタイヤケース半体同士を、互いに向かい合わせてタイヤ赤道面部分で接合することで、タイヤケースを形成する(接合工程)。なお、タイヤケースは、2つの部材を接合して形成するものに限らず、3以上の部材を接合して形成してもよい。
接合について説明する。まず、薄い金属の支持リングに支持されたタイヤケース半体同士を互いに向かい合わせる。次いで、タイヤケース半体の突き当て部分の外周面と接するように、接合金型を設置する。接合金型は、タイヤケース半体の接合部(つまり突き当て部分)周辺を、所定の圧力で押圧するように構成されている。次いで、タイヤケース半体の接合部周辺を、タイヤケースを形成する樹脂材料の融点以上の温度で押圧することで、接合部が溶融され、タイヤケース半体同士が融着して一体となり、タイヤケース17が形成される。
例えば、この接合工程において、樹脂材料の温度、例えば接合金型の温度等を調整することでも、タイヤケース17の非晶部の厚みLa、長周期L、配向度f、及び結晶化度Xc等を前述の範囲となるよう制御することができる。
第一実施形態の製造方法では、接合金型を用いてタイヤケース半体の接合部を加熱したが、本開示はこれに限定されない。例えば、別に設けた高周波加熱機等によって接合部を加熱したり、予め熱風、又は赤外線の照射等によって軟化または溶融させ、接合金型によって加圧してタイヤケース半体を接合させてもよい。
接合について説明する。まず、薄い金属の支持リングに支持されたタイヤケース半体同士を互いに向かい合わせる。次いで、タイヤケース半体の突き当て部分の外周面と接するように、接合金型を設置する。接合金型は、タイヤケース半体の接合部(つまり突き当て部分)周辺を、所定の圧力で押圧するように構成されている。次いで、タイヤケース半体の接合部周辺を、タイヤケースを形成する樹脂材料の融点以上の温度で押圧することで、接合部が溶融され、タイヤケース半体同士が融着して一体となり、タイヤケース17が形成される。
例えば、この接合工程において、樹脂材料の温度、例えば接合金型の温度等を調整することでも、タイヤケース17の非晶部の厚みLa、長周期L、配向度f、及び結晶化度Xc等を前述の範囲となるよう制御することができる。
第一実施形態の製造方法では、接合金型を用いてタイヤケース半体の接合部を加熱したが、本開示はこれに限定されない。例えば、別に設けた高周波加熱機等によって接合部を加熱したり、予め熱風、又は赤外線の照射等によって軟化または溶融させ、接合金型によって加圧してタイヤケース半体を接合させてもよい。
(補強コード部材巻回工程)
次に、補強コード26をタイヤケース17に巻回する巻回工程について、図3を用いて説明する。図3は、コード加熱装置、およびローラ類を用いてタイヤケース17のクラウン部に補強コード26を埋設する動作を説明するための説明図である。
図3において、コード供給装置56は、補強コード26を巻き付けたリール58と、リール58のコード搬送方向下流側に配置されたコード加熱装置59と、補強コード26の搬送方向下流側に配置された第1のローラ60と、第1のローラ60をタイヤ外周面に対して接離する方向に移動する第1のシリンダ装置62と、第1のローラ60の補強コード26の搬送方向下流側に配置される第2のローラ64と、第2のローラ64をタイヤ外周面に対して接離する方向に移動する第2のシリンダ装置66と、を備えている。第2のローラ64は、金属製の冷却用ローラとして利用することができる。
第一実施形態において、第1のローラ60または第2のローラ64の表面は、溶融または軟化した被覆用樹脂材料27の付着を抑制するための処理(例えば、フッ素樹脂コーティング)が施されている。ただし、この態様に限られず、ローラ自体を被覆用樹脂材料27が付着しにくい材料から形成してもよい。なお、第一実施形態では、コード供給装置56は、第1のローラ60及び第2のローラ64の2つのローラを有しているが、この態様に限られず、何れか一方のローラのみを有していてもよい。
次に、補強コード26をタイヤケース17に巻回する巻回工程について、図3を用いて説明する。図3は、コード加熱装置、およびローラ類を用いてタイヤケース17のクラウン部に補強コード26を埋設する動作を説明するための説明図である。
図3において、コード供給装置56は、補強コード26を巻き付けたリール58と、リール58のコード搬送方向下流側に配置されたコード加熱装置59と、補強コード26の搬送方向下流側に配置された第1のローラ60と、第1のローラ60をタイヤ外周面に対して接離する方向に移動する第1のシリンダ装置62と、第1のローラ60の補強コード26の搬送方向下流側に配置される第2のローラ64と、第2のローラ64をタイヤ外周面に対して接離する方向に移動する第2のシリンダ装置66と、を備えている。第2のローラ64は、金属製の冷却用ローラとして利用することができる。
第一実施形態において、第1のローラ60または第2のローラ64の表面は、溶融または軟化した被覆用樹脂材料27の付着を抑制するための処理(例えば、フッ素樹脂コーティング)が施されている。ただし、この態様に限られず、ローラ自体を被覆用樹脂材料27が付着しにくい材料から形成してもよい。なお、第一実施形態では、コード供給装置56は、第1のローラ60及び第2のローラ64の2つのローラを有しているが、この態様に限られず、何れか一方のローラのみを有していてもよい。
コード加熱装置59は、熱風を生じさせるヒーター70およびファン72を備えている。また、コード加熱装置59は、内部に熱風が供給される内部空間を、補強コード26が通過する加熱ボックス74と、加熱された補強コード26を排出する排出口76と、を備えている。
本工程においては、まず、コード加熱装置59のヒーター70の温度を上昇させ、ヒーター70で加熱された周囲の空気を、ファン72の回転によって生じる風で加熱ボックス74へ送る。次に、リール58から巻き出した補強コード26を、熱風で内部空間が加熱された加熱ボックス74内へ送り、加熱する。加熱の温度は、補強コード26の被覆用樹脂材料27が溶融または軟化した状態となる温度に設定する。
加熱された補強コード26は、排出口76を通り、図3の矢印R方向に回転するタイヤケース17のクラウン部16の外周面に、一定のテンションをもって螺旋状に巻きつけられる。このとき、クラウン部16の外周面に、補強コード26の下面26Dが接触する。そして、加熱により溶融または軟化した状態の被覆用樹脂材料27がクラウン部16の外周面上に広がり、クラウン部16の外周面に補強コード26が溶着される。これにより、クラウン部16と補強コード26との接合強度が向上する。
第一実施形態では、上述のようにしてクラウン部16の外周面に補強コード26を接合したが、この態様に限られず、他の方法で接合を行ってもよい。例えば、補強コード26の一部又は全体がクラウン部16に埋設されるように接合を行ってもよい。
(粗化処理工程)
次に、図示を省略するブラスト装置にて、タイヤケース17の外周面17Sに向け、タイヤケース17側を回転させながら、外周面17Sへ投射材を高速度で射出する。射出された投射材は、外周面17Sに衝突し、この外周面17Sに算術平均粗さRaが0.05mm以上となる微細な粗化凹凸96を形成する。タイヤケース17の外周面17Sに微細な粗化凹凸96が形成されることで、外周面17Sが親水性となり、後述する接合剤の濡れ性が向上する。
次に、図示を省略するブラスト装置にて、タイヤケース17の外周面17Sに向け、タイヤケース17側を回転させながら、外周面17Sへ投射材を高速度で射出する。射出された投射材は、外周面17Sに衝突し、この外周面17Sに算術平均粗さRaが0.05mm以上となる微細な粗化凹凸96を形成する。タイヤケース17の外周面17Sに微細な粗化凹凸96が形成されることで、外周面17Sが親水性となり、後述する接合剤の濡れ性が向上する。
(積層工程)
次に、粗化処理を行なったタイヤケース17の外周面17Sに、クッションゴム29を接合するための接合剤を塗布する。接合剤は特に制限されず、トリアジンチオール系接着剤、塩化ゴム系接着剤、フェノール系樹脂接着剤、イソシアネート系接着剤、ハロゲン化ゴム系接着剤、及びゴム系接着剤等を用いることができる。ただし、クッションゴム29が加硫できる温度(例えば90℃~140℃)で反応するものであることが好ましい。
次に、粗化処理を行なったタイヤケース17の外周面17Sに、クッションゴム29を接合するための接合剤を塗布する。接合剤は特に制限されず、トリアジンチオール系接着剤、塩化ゴム系接着剤、フェノール系樹脂接着剤、イソシアネート系接着剤、ハロゲン化ゴム系接着剤、及びゴム系接着剤等を用いることができる。ただし、クッションゴム29が加硫できる温度(例えば90℃~140℃)で反応するものであることが好ましい。
次に、接合剤が塗布された外周面17Sに未加硫状態のクッションゴム29を1周分巻き付け、クッションゴム29の上にゴムセメント組成物等の接合剤を塗布する。次いで、接合剤が塗布されたクッションゴム29の上に、加硫済みまたは半加硫状態のトレッドゴム30Aを1周分巻き付けて、生タイヤケースの状態とする。
(加硫工程)
次に、生タイヤケースを加硫缶やモールドに収容して加硫する。このとき、粗化処理によってタイヤケース17の外周面17Sに形成された粗化凹凸96に未加硫のクッションゴム29が流れ込む。そして、加硫が完了すると、粗化凹凸96に流れ込んだクッションゴム29により、アンカー効果が発揮されて、タイヤケース17とクッションゴム29との接合強度が向上する。すなわち、クッションゴム29を介してタイヤケース17とトレッド30との接合強度が向上する。
次に、生タイヤケースを加硫缶やモールドに収容して加硫する。このとき、粗化処理によってタイヤケース17の外周面17Sに形成された粗化凹凸96に未加硫のクッションゴム29が流れ込む。そして、加硫が完了すると、粗化凹凸96に流れ込んだクッションゴム29により、アンカー効果が発揮されて、タイヤケース17とクッションゴム29との接合強度が向上する。すなわち、クッションゴム29を介してタイヤケース17とトレッド30との接合強度が向上する。
そして、タイヤケース17のビード部12に、上述したシール層24を、接着剤等を用いて接着すれば、タイヤ10の完成となる。
以上、第一実施形態を例に挙げて本開示の実施の形態を説明したが、これらの実施形態は一例であり、要旨を逸脱しない範囲内で種々変更して実施できる。また、本発明の権利範囲がこれらの実施形態に限定されないことは言うまでもない。なお、本開示に適用可能な実施形態の詳細については、例えば、特開2012-46025号公報の記載を参照することができる。
上記の通り、本開示によれば以下のタイヤが提供される。
<1> 本開示の第1の観点によれば、熱可塑性エラストマーを含む樹脂材料で形成されたタイヤ骨格体を有し、
前記熱可塑性エラストマーの小角X線散乱法により測定される非晶部の厚みLaが12.3nm~13.9nmの範囲内であるタイヤが提供される。
<2> 本開示の第2の観点によれば、前記熱可塑性エラストマーの小角X線散乱法により測定される長周期Lが15.6nm~17.1nmの範囲内である、前記第1の観点によるタイヤが提供される。
<3> 本開示の第3の観点によれば、前記熱可塑性エラストマーの小角X線散乱法により測定される配向度fが-0.08~0.08の範囲内である、前記第1又は第2の観点によるタイヤが提供される。
<4> 本開示の第4の観点によれば、前記熱可塑性エラストマーがポリエステル系熱可塑性エラストマーである、前記第1~第3のいずれか1の観点によるタイヤが提供される。
<1> 本開示の第1の観点によれば、熱可塑性エラストマーを含む樹脂材料で形成されたタイヤ骨格体を有し、
前記熱可塑性エラストマーの小角X線散乱法により測定される非晶部の厚みLaが12.3nm~13.9nmの範囲内であるタイヤが提供される。
<2> 本開示の第2の観点によれば、前記熱可塑性エラストマーの小角X線散乱法により測定される長周期Lが15.6nm~17.1nmの範囲内である、前記第1の観点によるタイヤが提供される。
<3> 本開示の第3の観点によれば、前記熱可塑性エラストマーの小角X線散乱法により測定される配向度fが-0.08~0.08の範囲内である、前記第1又は第2の観点によるタイヤが提供される。
<4> 本開示の第4の観点によれば、前記熱可塑性エラストマーがポリエステル系熱可塑性エラストマーである、前記第1~第3のいずれか1の観点によるタイヤが提供される。
以下、本開示について実施例を用いてより具体的に説明する。ただし、本開示はこれに限定されるものではない。
[タイヤの作製]
各実施例及び比較例におけるタイヤとして、上述の第一実施形態に示した構成を有するタイヤを、公知の方法により作製した。タイヤ骨格体を形成する樹脂材料としては、ハードセグメントがポリエステルであり、ソフトセグメントがポリエーテルであるポリエステル系熱可塑性エラストマーを使用した。
各実施例及び比較例におけるタイヤとして、上述の第一実施形態に示した構成を有するタイヤを、公知の方法により作製した。タイヤ骨格体を形成する樹脂材料としては、ハードセグメントがポリエステルであり、ソフトセグメントがポリエーテルであるポリエステル系熱可塑性エラストマーを使用した。
なお、各実施例及び比較例でのタイヤケース半体の成形にあたっては、射出成形時のシリンダの温度、金型温度、冷却速度、及び冷却時間を、表1に記載の条件とした。
補強コードの作製は、まず平均直径が1.15mmのマルチフィラメント(具体的には平均直径が0.35mmの5本のモノフィラメント(スチール製、強力:280N、伸度:3%)を撚った撚り線)に、加熱溶融した酸変性ポリプロピレンを付着させて接着層を形成した。次いで、接着層の上を、押出機にて押し出したポリアミド系熱可塑性エラストマー(UBE(株)製、商品名「XPA9055」)で被覆し、冷却することで、補強コードを作製した。
・非晶部の厚みLa、長周期L、配向度f、及び結晶化度Xcの測定
作製したタイヤのタイヤケースから作製したサンプルを用いて、熱可塑性エラストマーの非晶部の厚みLa、長周期L、及び配向度fを、小角X線散乱法により測定し、また結晶化度Xcを広角X線散乱法により測定した。
なお、測定装置としては(株)リガク社製の製品名:Nano-Viewerを用い、測定条件を以下の通り調整した。
-測定条件-
・室温測定
・X線照射時間30分
測定結果を表1に示す。
作製したタイヤのタイヤケースから作製したサンプルを用いて、熱可塑性エラストマーの非晶部の厚みLa、長周期L、及び配向度fを、小角X線散乱法により測定し、また結晶化度Xcを広角X線散乱法により測定した。
なお、測定装置としては(株)リガク社製の製品名:Nano-Viewerを用い、測定条件を以下の通り調整した。
-測定条件-
・室温測定
・X線照射時間30分
測定結果を表1に示す。
[耐久性の評価]
実施例及び比較例で作製したタイヤの耐久性の評価を、下記に示す耐亀裂進展性(亀裂成長速度DC/DNの測定)、及びBFドラム試験によって実施した。結果を表1に示す。
実施例及び比較例で作製したタイヤの耐久性の評価を、下記に示す耐亀裂進展性(亀裂成長速度DC/DNの測定)、及びBFドラム試験によって実施した。結果を表1に示す。
-耐亀裂進展性(亀裂成長速度DC/DNの測定)-
作製したタイヤのタイヤケースから作製したサンプルから、JIS K6251:1993に規定されるダンベル状試験片(7号形試験片)を作製した。
作製した試験片に0.5mmの予亀裂を付け、亀裂成長速度DC/DN〔mm/cycle〕を、(株)島津製作所の電磁式サーボパルサーにて測定した。測定条件は、温度=40℃、歪=3%、周波数=17Hzとした。なお、値が大きい方が耐亀裂進展性に優れる。
作製したタイヤのタイヤケースから作製したサンプルから、JIS K6251:1993に規定されるダンベル状試験片(7号形試験片)を作製した。
作製した試験片に0.5mmの予亀裂を付け、亀裂成長速度DC/DN〔mm/cycle〕を、(株)島津製作所の電磁式サーボパルサーにて測定した。測定条件は、温度=40℃、歪=3%、周波数=17Hzとした。なお、値が大きい方が耐亀裂進展性に優れる。
-BFドラム試験-
上述の方法にてサイズ195/65R15の試作タイヤを作製し、前記試作タイヤを25±2℃の室内中で内圧3.0kg/cm2に調整した後、24時間放置した。その後、空気圧の再調整を行い、540Kgの荷重をタイヤに負荷し、直径約3mのドラム上で速度60km/時で2万km走行させ、以下の基準により評価した。評価結果が「A」又は「B」であればタイヤとしての使用に好適であると言える。
「A」:走行後、亀裂等の外傷が見られなかったもの
「B」:完走できたものの走行に支障のない程度の亀裂等の外傷が見られたもの
「C」:完走できなかったもの、又は走行に支障をきたす亀裂等の外傷があったもの
上述の方法にてサイズ195/65R15の試作タイヤを作製し、前記試作タイヤを25±2℃の室内中で内圧3.0kg/cm2に調整した後、24時間放置した。その後、空気圧の再調整を行い、540Kgの荷重をタイヤに負荷し、直径約3mのドラム上で速度60km/時で2万km走行させ、以下の基準により評価した。評価結果が「A」又は「B」であればタイヤとしての使用に好適であると言える。
「A」:走行後、亀裂等の外傷が見られなかったもの
「B」:完走できたものの走行に支障のない程度の亀裂等の外傷が見られたもの
「C」:完走できなかったもの、又は走行に支障をきたす亀裂等の外傷があったもの

表1に記載の熱可塑性エラストマーの詳細を、以下に示す。
・Hytrel5557(ポリエステル系熱可塑性エラストマー、東レ・デュポン(株)製、結晶化温度:163℃)
・Hytrel4767N(ポリエステル系熱可塑性エラストマー、東レ・デュポン(株)製、結晶化温度:155℃)
なお、実施例6では、Hytrel5557とHytrel4767Nとを、質量比で「25/75」の割合で混合して用いた。
・Hytrel5557(ポリエステル系熱可塑性エラストマー、東レ・デュポン(株)製、結晶化温度:163℃)
・Hytrel4767N(ポリエステル系熱可塑性エラストマー、東レ・デュポン(株)製、結晶化温度:155℃)
なお、実施例6では、Hytrel5557とHytrel4767Nとを、質量比で「25/75」の割合で混合して用いた。
表1に示されるように、非晶部の厚みLaが12.3nm~13.9nmの範囲内にある熱可塑性エラストマーを用いて形成したタイヤケースを有する実施例のタイヤは、非晶部の厚みLaが上記範囲内にない熱可塑性エラストマーを用いて形成したタイヤケースを有する比較例のタイヤに比べて、耐久性に優れていることが分かる。
なお、日本出願2017-082200の開示はその全体が参照により本明細書に取り込まれる。
本明細書に記載された全ての文献、特許出願、および技術規格は、個々の文献、特許出願、および技術規格が参照により取り込まれることが具体的かつ個々に記された場合と同程度に、本明細書中に参照により取り込まれる。
本明細書に記載された全ての文献、特許出願、および技術規格は、個々の文献、特許出願、および技術規格が参照により取り込まれることが具体的かつ個々に記された場合と同程度に、本明細書中に参照により取り込まれる。
Claims (4)
- 熱可塑性エラストマーを含む樹脂材料で形成されたタイヤ骨格体を有し、
前記熱可塑性エラストマーの小角X線散乱法により測定される非晶部の厚みLaが12.3nm~13.9nmの範囲内であるタイヤ。 - 前記熱可塑性エラストマーの小角X線散乱法により測定される長周期Lが15.6nm~17.1nmの範囲内である請求項1に記載のタイヤ。
- 前記熱可塑性エラストマーの小角X線散乱法により測定される配向度fが-0.08~0.08の範囲内である請求項1又は請求項2に記載のタイヤ。
- 前記熱可塑性エラストマーがポリエステル系熱可塑性エラストマーである請求項1~請求項3のいずれか1項に記載のタイヤ。
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP18787330.2A EP3613611A4 (en) | 2017-04-18 | 2018-03-29 | PNEUMATIC |
| CN201880025491.1A CN110546018B (zh) | 2017-04-18 | 2018-03-29 | 轮胎 |
| US16/653,160 US20200039292A1 (en) | 2017-04-18 | 2019-10-15 | Tire |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2017082200A JP6817879B2 (ja) | 2017-04-18 | 2017-04-18 | タイヤ |
| JP2017-082200 | 2017-04-18 |
Related Child Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| US16/653,160 Continuation US20200039292A1 (en) | 2017-04-18 | 2019-10-15 | Tire |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2018193811A1 true WO2018193811A1 (ja) | 2018-10-25 |
Family
ID=63856614
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2018/013439 Ceased WO2018193811A1 (ja) | 2017-04-18 | 2018-03-29 | タイヤ |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US20200039292A1 (ja) |
| EP (1) | EP3613611A4 (ja) |
| JP (1) | JP6817879B2 (ja) |
| CN (1) | CN110546018B (ja) |
| WO (1) | WO2018193811A1 (ja) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP7688515B2 (ja) * | 2021-05-06 | 2025-06-04 | 株式会社ブリヂストン | タイヤ及びタイヤ骨格体の製造方法 |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH05331256A (ja) | 1992-06-02 | 1993-12-14 | Sanko Chem Co Ltd | 熱可塑性ポリウレタンの製造方法 |
| JP2000191928A (ja) * | 1998-12-28 | 2000-07-11 | Sumitomo Rubber Ind Ltd | ボ―ル用熱可塑性樹脂組成物及びこれを用いたワンピ―スゴルフボ―ル |
| JP2004346273A (ja) | 2003-05-26 | 2004-12-09 | Ube Ind Ltd | ポリアミド系エラストマー及びその製造方法 |
| WO2008026509A1 (en) * | 2006-08-29 | 2008-03-06 | National Institute Of Advanced Industrial Science And Technology | Thermoplastic elastomer composition having hierarchical structure and process for the production thereof |
| JP2008308636A (ja) * | 2007-06-18 | 2008-12-25 | Toyobo Co Ltd | 熱可塑性ポリエステルエラストマー |
| WO2011074473A1 (ja) * | 2009-12-14 | 2011-06-23 | アロン化成株式会社 | 熱可塑性エラストマー組成物及びその製造方法 |
| JP2012046025A (ja) | 2010-08-25 | 2012-03-08 | Bridgestone Corp | タイヤ |
| JP2014198779A (ja) * | 2013-03-29 | 2014-10-23 | 株式会社ブリヂストン | タイヤ |
| JP2017082200A (ja) | 2015-09-30 | 2017-05-18 | 京セラ株式会社 | 樹脂組成物、プリプレグ、金属張積層板、および配線基板 |
| WO2017146038A1 (ja) * | 2016-02-26 | 2017-08-31 | 株式会社ブリヂストン | タイヤ |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP5893439B2 (ja) * | 2012-02-29 | 2016-03-23 | 株式会社ブリヂストン | タイヤの製造方法 |
| US20170298182A1 (en) * | 2014-09-24 | 2017-10-19 | Bridgestone Corporation | Tire |
-
2017
- 2017-04-18 JP JP2017082200A patent/JP6817879B2/ja active Active
-
2018
- 2018-03-29 WO PCT/JP2018/013439 patent/WO2018193811A1/ja not_active Ceased
- 2018-03-29 EP EP18787330.2A patent/EP3613611A4/en not_active Withdrawn
- 2018-03-29 CN CN201880025491.1A patent/CN110546018B/zh active Active
-
2019
- 2019-10-15 US US16/653,160 patent/US20200039292A1/en not_active Abandoned
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH05331256A (ja) | 1992-06-02 | 1993-12-14 | Sanko Chem Co Ltd | 熱可塑性ポリウレタンの製造方法 |
| JP2000191928A (ja) * | 1998-12-28 | 2000-07-11 | Sumitomo Rubber Ind Ltd | ボ―ル用熱可塑性樹脂組成物及びこれを用いたワンピ―スゴルフボ―ル |
| JP2004346273A (ja) | 2003-05-26 | 2004-12-09 | Ube Ind Ltd | ポリアミド系エラストマー及びその製造方法 |
| WO2008026509A1 (en) * | 2006-08-29 | 2008-03-06 | National Institute Of Advanced Industrial Science And Technology | Thermoplastic elastomer composition having hierarchical structure and process for the production thereof |
| JP2008308636A (ja) * | 2007-06-18 | 2008-12-25 | Toyobo Co Ltd | 熱可塑性ポリエステルエラストマー |
| WO2011074473A1 (ja) * | 2009-12-14 | 2011-06-23 | アロン化成株式会社 | 熱可塑性エラストマー組成物及びその製造方法 |
| JP2012046025A (ja) | 2010-08-25 | 2012-03-08 | Bridgestone Corp | タイヤ |
| JP2014198779A (ja) * | 2013-03-29 | 2014-10-23 | 株式会社ブリヂストン | タイヤ |
| JP2017082200A (ja) | 2015-09-30 | 2017-05-18 | 京セラ株式会社 | 樹脂組成物、プリプレグ、金属張積層板、および配線基板 |
| WO2017146038A1 (ja) * | 2016-02-26 | 2017-08-31 | 株式会社ブリヂストン | タイヤ |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP3613611A4 |
Also Published As
| Publication number | Publication date |
|---|---|
| EP3613611A4 (en) | 2020-11-25 |
| JP6817879B2 (ja) | 2021-01-20 |
| JP2018177091A (ja) | 2018-11-15 |
| CN110546018A (zh) | 2019-12-06 |
| US20200039292A1 (en) | 2020-02-06 |
| CN110546018B (zh) | 2021-12-07 |
| EP3613611A1 (en) | 2020-02-26 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP6057981B2 (ja) | タイヤ | |
| JP6086643B2 (ja) | タイヤ | |
| JP5818577B2 (ja) | タイヤ | |
| JP6138412B2 (ja) | タイヤ | |
| WO2013129632A1 (ja) | タイヤ | |
| JP5847555B2 (ja) | タイヤ | |
| JP2013220692A (ja) | タイヤ | |
| WO2019230822A1 (ja) | タイヤ用樹脂金属複合部材、及びその製造方法、並びにタイヤ | |
| WO2017104484A1 (ja) | タイヤ | |
| JP5818578B2 (ja) | タイヤ | |
| JP5911731B2 (ja) | タイヤ | |
| JP5778402B2 (ja) | タイヤ | |
| JP5627954B2 (ja) | タイヤ | |
| JP6014713B2 (ja) | タイヤ | |
| CN108495890B (zh) | 轮胎 | |
| JP5993544B2 (ja) | タイヤ | |
| JP6817879B2 (ja) | タイヤ | |
| JP7688515B2 (ja) | タイヤ及びタイヤ骨格体の製造方法 | |
| JP5905566B2 (ja) | タイヤ | |
| JP6014714B2 (ja) | タイヤ及びその製造方法 | |
| WO2017104483A1 (ja) | タイヤ | |
| WO2017104187A1 (ja) | タイヤ | |
| US20200238762A1 (en) | Tire | |
| JP2019001358A (ja) | タイヤ |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 18787330 Country of ref document: EP Kind code of ref document: A1 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 2018787330 Country of ref document: EP Effective date: 20191118 |