WO2019172443A1 - 光ファイバテープ心線及び光ファイバケーブル - Google Patents
光ファイバテープ心線及び光ファイバケーブル Download PDFInfo
- Publication number
- WO2019172443A1 WO2019172443A1 PCT/JP2019/009481 JP2019009481W WO2019172443A1 WO 2019172443 A1 WO2019172443 A1 WO 2019172443A1 JP 2019009481 W JP2019009481 W JP 2019009481W WO 2019172443 A1 WO2019172443 A1 WO 2019172443A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- optical fiber
- viscosity
- intermittent connection
- core wire
- shear rate
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images



Classifications
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/44—Mechanical structures for providing tensile strength and external protection for fibres, e.g. optical transmission cables
- G02B6/4401—Optical cables
- G02B6/4403—Optical cables with ribbon structure
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/44—Mechanical structures for providing tensile strength and external protection for fibres, e.g. optical transmission cables
- G02B6/4401—Optical cables
- G02B6/4403—Optical cables with ribbon structure
- G02B6/4404—Multi-podded
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/44—Mechanical structures for providing tensile strength and external protection for fibres, e.g. optical transmission cables
- G02B6/4401—Optical cables
- G02B6/4429—Means specially adapted for strengthening or protecting the cables
- G02B6/44384—Means specially adapted for strengthening or protecting the cables the means comprising water blocking or hydrophobic materials
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/44—Mechanical structures for providing tensile strength and external protection for fibres, e.g. optical transmission cables
- G02B6/4479—Manufacturing methods of optical cables
- G02B6/448—Ribbon cables
-
- G—PHYSICS
- G02—OPTICS
- G02B—OPTICAL ELEMENTS, SYSTEMS OR APPARATUS
- G02B6/00—Light guides; Structural details of arrangements comprising light guides and other optical elements, e.g. couplings
- G02B6/44—Mechanical structures for providing tensile strength and external protection for fibres, e.g. optical transmission cables
- G02B6/4479—Manufacturing methods of optical cables
- G02B6/4482—Code or colour marking
Definitions
- the present invention relates to an optical fiber ribbon and an optical fiber cable. More specifically, the optical fiber ribbon and the optical fiber ribbon are formed by intermittently adhering and connecting adjacent optical fiber colored cores to each other in the longitudinal direction and the tape width direction by an intermittent connection portion. Relates to optical fiber cables.
- optical fiber cables are also required to have a smaller diameter and higher density.
- optical fiber ribbons have been proposed in order to realize a reduction in the diameter and density of the optical fiber cable.
- the adjacent optical fibers are intermittently connected in the longitudinal direction to obtain a tape width.
- optical fiber ribbon that is alternately arranged so that connecting portions adjacent in the direction do not overlap (see, for example, Patent Document 1).
- the optical fiber tape core wire is made of an ultraviolet curable resin or the like, in which a plurality of optical fiber core wires (optical fiber colored core wires) obtained by applying a protective coating to the optical fiber with an ultraviolet curable resin or the like are arranged in a planar shape. It is connected and integrated at the connecting portion.
- Japanese Patent No. 5117519 JP 2001-264604 A Japanese Patent No. 5149230 Japanese Patent No. 6169060
- an operation of applying a resin between the optical fiber colored core wires and the optical fiber colored core wires Must be synchronized. Therefore, in order to manufacture an optical fiber ribbon with a high linear velocity (for example, a linear velocity of 200 m / min or more as the linear velocity of an optical fiber colored core), the viscosity at the time of applying a resin, The ease of resin wear is greatly affected.
- the present invention has been made in view of the above-described problems, and is an intermittently connected optical fiber tape core formed by adhering and connecting adjacent optical fiber colored cores with an intermittently connected portion at a high speed.
- An object of the present invention is to provide an optical fiber ribbon and an optical fiber cable that can be manufactured.
- an optical fiber ribbon according to the present invention has at least two coating layers covering the optical fiber formed around the optical fiber, and the outermost layer of the coating layers is colored.
- the optical fiber colored cores configured in parallel are arranged in parallel, and the adjacent optical fiber colored cores are optical fiber tape cores connected in the length direction by intermittent connection parts, and the intermittent connection parts
- a rheology control agent containing a polyol having a weight average molecular weight of 2500 to 4000 and shifting the Newton region between the low shear rate region and the high shear rate region to the high shear region side is applied to the entire intermittent connection portion. 1 to 10% by mass.
- the optical fiber ribbon according to the present invention is characterized in that, in the above-described present invention, the intermittent connection portion contains 4 to 30% by mass of the polyol with respect to the entire intermittent connection portion.
- the optical fiber ribbon according to the present invention is characterized in that, in the above-described present invention, the rheology control agent is hydrophobic fumed silica.
- the viscosity of the material forming the intermittent connection portion is a shear rate of 10 1 1 / s determined from dynamic viscoelasticity at 25 ° C.
- the viscosity is 3 to 11 Pa ⁇ s
- the viscosity at a shear rate of 10 6 1 / s determined from dynamic viscoelasticity at 25 ° C. is 0.2 to 2.5 Pa ⁇ s.
- the optical fiber ribbon according to the present invention is determined from the viscosity at a shear rate of 10 1 1 / s determined from the dynamic viscoelasticity at 25 ° C. and the dynamic viscoelasticity at 35 ° C. in the above-described present invention. Furthermore, the ratio of the viscosity at a shear rate of 10 1 1 / s (viscosity at 25 ° C./viscosity at 35 ° C.) is 3 or less.
- the optical fiber ribbon according to the present invention is characterized in that an adhesive strength between the optical fiber colored core and the intermittent connection portion is 0.07 N or more.
- An optical fiber cable according to the present invention includes the above-described optical fiber tape core wire of the present invention.
- the optical fiber ribbon of the present invention contains a polyol having a weight average molecular weight of 2500 to 4000 with respect to the material constituting the intermittently connected portion (ultraviolet curable resin composition), and also has a specific rheology control agent. Contains in a range. With this configuration, the material constituting the intermittent connection portion has a relatively high viscosity in the low shear rate region and a relatively low viscosity in the high shear rate region, whereas the material constituting the intermittent connection portion has a high shear rate region of 10 6.
- the centrifugal force generated by the rotation of the coating roll that applies the material at the time of manufacture can be suppressed by the force, and the amount applied to the optical fiber colored core can be stabilized. And it becomes an optical fiber cable provided with the optical fiber tape core wire and the said optical fiber colored core wire which can maintain suppression of this scattering etc. also at high-speed manufacture.
- the optical fiber ribbon 2 according to the present invention, at least two coating layers that cover the optical fiber 10 are formed around the optical fiber 10, and the outermost layer of the coating layers is colored.
- the colored core wires 1 are arranged in parallel, and the adjacent optical fiber colored core wires 1 are intermittently connected in the length direction by the intermittent connecting portion 3.
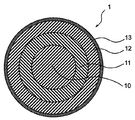
- FIG. 1 is a cross-sectional view showing an example of the structure of the optical fiber colored core wire 1.
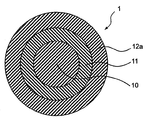
- FIG. 2 is a cross-sectional view showing another example of the structure of the optical fiber colored core wire 1.
- 1 and 2 1 is an optical fiber colored core wire, 10 is an optical fiber, 11 is a primary coating layer, 12 is a secondary coating layer, 12a is a colored secondary coating layer (FIG. 2 only), 13 is Colored layers (FIG. 1 only) are shown respectively.
- a primary coating layer 11 (primary layer) around an optical fiber 10 such as a glass optical fiber
- a secondary coating layer 12 (secondary layer) around the primary coating layer 11, and a secondary coating layer.
- a colored layer 13 colored around 12 is formed in this order, and constitutes the optical fiber colored core wire 1.
- the colored layer 13 is the outermost layer of the optical fiber colored core wire 1.
- a primary coating layer 11 and a secondary coating layer 12a colored around the primary coating layer 11 are formed around the optical fiber 10 in this order.
- the colored secondary coating layer 12 a is the outermost layer of the optical fiber colored core wire 1.
- the colored layer 13 that is the outermost layer of the optical fiber colored core wire 1 and the colored secondary coating layer 12a may be combined to form the colored layer 13 or the like.
- FIG. 3 is a front view showing an aspect of the optical fiber ribbon 2.
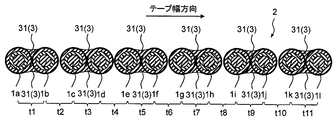
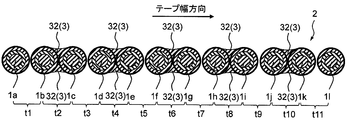
- 4 and 5 are diagrams showing the connection state of the optical fiber ribbon 2 (FIG. 4 is a cross-sectional view taken along the line AA in FIG. 3 including the intermittent connection portion 31, and FIG. Is a cross-sectional view taken along the line BB of FIG. 3 to 5 show an optical fiber ribbon 2 composed of 12 optical fiber colored cores 1 for convenience.
- the intermittently connected optical fiber tape core 2 is an optical fiber colored core wire 1 arranged in parallel. It is also called intermittent connection in the length direction.
- the connecting portion intermittent connecting portion 3
- the optical fiber colored core wires 1 can be connected and integrated.
- a pair of optical fiber colored cores t1 composed of the optical fiber colored core 1a and the optical fiber colored core 1b is lengthened by the intermittent connecting portion 31. (See FIG. 3).
- adjacent intermittent connection portions 31 can be provided at equal intervals, and the lengths of the intermittent connection portions 31 can also be made equal.
- optical fiber colored core wire pair t3 consisting of optical fiber colored core wire 1c and optical fiber colored core wire 1d
- optical fiber colored core wire pair t5 consisting of optical fiber colored core wire 1e and optical fiber colored core wire 1f
- An optical fiber colored core pair t7 composed of an optical fiber colored core 1g and an optical fiber colored core 1h
- an optical fiber colored core t9 composed of an optical fiber colored core 1i and an optical fiber colored core 1j
- an optical fiber colored core is the same applies to the optical fiber colored core pair t11 including the line 1k and the optical fiber colored core 1l.
- intermittent coupling portions 31 are provided so that the arrangement in the tape width direction is the same (see FIG. 3). ). Therefore, the non-connected portion (single-core portion where the intermittently connected portion 3 is not formed) of the six pairs of optical fiber colored core wires t1, t3, t5, t7, t9, and t11 is shown in FIG.
- the portion surrounded by the dotted line.) 33 is also a common position when viewed from the tape width direction.
- the optical fiber colored core wire pair t2 composed of the optical fiber colored core wire 1b and the optical fiber colored core wire 1c is intermittently connected in the length direction by the intermittent connecting portion 32.
- the adjacent intermittent connection parts 32 can be provided at equal intervals, and the lengths of the intermittent connection parts 32 can also be made equal.
- optical fiber colored core wire pair t6 consisting of optical fiber colored core wire 1d and optical fiber colored core wire 1e
- optical fiber colored core wire pair t6 consisting of optical fiber colored core wire 1f and optical fiber colored core wire 1g
- optical fiber colored core wire t8 composed of the optical fiber colored core wire 1h and the optical fiber colored core wire 1i
- optical fiber colored core wire pair t10 composed of the optical fiber colored core wire 1j and the optical fiber colored core wire 1k.
- intermittent coupling portions 32 are provided so that the arrangement in the tape width direction is the same. Therefore, the unconnected portions 33 of the five pairs of optical fiber colored cores t2, t4, t6, t8, and t10 are also in a common position when viewed from the tape width direction.
- the intermittently connected optical fiber ribbon 2 is not separated from the intermittently connected portions 31 and 32 in the length direction and the tape width direction with respect to the adjacent two (two) optical fiber colored cores 1.
- the connecting portions 33 are formed so as to be alternately arranged with a predetermined length, and the adjacent optical fiber colored core wires 1 are intermittently connected in the length direction by the intermittent connecting portion 3 (for example, FIG. 3).
- An optical fiber colored core wire t1 composed of the optical fiber colored core wire 1a and the optical fiber colored core wire 1b, an optical fiber colored core wire pair t2 composed of the optical fiber colored core wire 1b and the optical fiber colored core wire 1c, etc. reference.).
- intermittent pairs of optical fiber colored core pairs t1 to t11 composed of two adjacent cores (two) formed with intermittent coupling portions 31 and 32 are formed. Both sides (outside) in the tape width direction of the portion where the connecting portion 3 is formed are not connected (for example, from the optical fiber colored core 1c and the optical fiber colored core 1d shown in FIG. 4).
- the optical fiber colored core pair t3 is formed with an intermittent coupling portion 31 that couples the two optical fiber colored core wires 1c and 1d, while a portion in which the intermittent coupling portion 3 is formed in the tape width direction. Both sides (outside) are not connected.
- the length L1 of the intermittent connection portions 31 and 32 in the optical fiber ribbon 2 is preferably about 5 to 35 mm, and the length of the non-connection portion 33 is The length L2 is preferably about 5 to 15 mm.
- the pitch P in the optical fiber ribbon 2 indicates the length of the intermittent connection part 31 to the intermittent connection part 31 (or the intermittent connection part 32 to the intermittent connection part 32) adjacent in the length direction.
- the portion 31 to the intermittently connected portion 31) is preferably 100 mm or less, and generally preferably 20 to 90 mm, but is not particularly limited to this range.
- the non-connecting portion refers to a single core portion (single core portion) where the intermittent connecting portion 3 is not formed.
- X shown in FIG. 3 is also a non-connecting portion (non-connecting portion X having a length LX).
- LX of the pair of optical fiber colored core wires is LX.
- the thickness is preferably 15 to 55 mm, but is not particularly limited to this range.
- the intermittently connecting portion 3 shown in FIG. 3 and the like can be formed by curing the following components, for example.
- the component constituting the intermittent connection portion 3 includes a polyol having a weight average molecular weight (M w ) of 2500 to 4000.
- the polyol having such a weight average molecular weight (hereinafter sometimes simply referred to as “molecular weight”) can exist without reacting with the network of the ultraviolet curable resin constituting the intermittent connection portion 3.
- the intermittent connection part 3 is that the polyol is swollen in the dense network structure of the ultraviolet curable resin, and plays a role of a plasticizer for the ultraviolet curable resin.
- the Young's modulus of the intermittent connection part 3 moderate, flexibility and elongation can be provided to the intermittent connection part 3 also under low temperature conditions. Further, the polyol can bleed on the surface of the intermittent connection portion 3 to suppress friction between the optical fiber units 21.
- the weight average molecular weight of the polyol is in the above-described range, it is considered that the molecular weight of the colored layer 13 of the optical fiber colored core wire 1 is larger, so that the colored layer 13 does not pass through the mesh and does not move.
- the molecular weight of the polyol is as large as 2500 to 4000, it is possible to control the Young's modulus of the intermittent connection portion 3 by increasing the polyol content. As described above, the presence of the polyol in the intermittent connection portion 3 can impart flexibility and elongation to the intermittent connection portion 3 even under a low temperature condition, and the polyol bleeds on the surface of the intermittent connection portion 3. The friction between the optical fiber units 21 can be suppressed.
- polyol examples include polypropylene glycol, polyethylene glycol, and polytetramethylene glycol.
- those having no branched structure such as polyethylene glycol and polytetramethylene glycol are crystallized at low temperatures. There is a case where bending due to crystals occurs at the interface between the colored layer 13 and the intermittent coupling portion 3 and causes an increase in loss.
- polypropylene glycol having a branched structure does not crystallize even at a low temperature of ⁇ 60 ° C., and the above-described effects of the polyol can be reliably obtained. Therefore, it is preferable to use polypropylene glycol as the polyol.
- Polypropylene glycol is produced by addition polymerization of polypropylene oxide (PO) to polyfunctional alcohol using an alkali catalyst, but ethylene oxide (EO) may be added and used to enhance the reaction, but ethylene oxide is added. Then, since hydrophilicity becomes high, it is preferable to use only polypropylene oxide (PO) as an additional substance.
- PO polypropylene oxide
- EO ethylene oxide
- the weight average molecular weight of the polyol contained in the intermittent connection part 3 is 2500 to 4000.
- the weight average molecular weight of the polyol is smaller than 2500, the polyol may migrate through the colored layer 13 in contact with the intermittent connection portion 3.
- it when it is set as the optical fiber cable 4, it may transfer to the buffer layer and coating layer (sheath) of the optical fiber cable which touches the intermittent connection part 3. Due to such a migration of polyol, the above-described effects may not be achieved.
- the viscosity increases when mixed with the ultraviolet curable resin, so that the coating amount when applying the intermittent connection part 3 at the time of manufacture is lowered, resulting in poor adhesion.
- the viscosity can be lowered by increasing the heating temperature or the like.
- the heating temperature is increased, the amount of resin at the time of application tends to increase, and the thickness of the intermittent connection portion 3 increases. It may be a factor.
- stringing may occur between the intermittently connected portion and the roll portion, which may be a factor that contaminates the surroundings.
- the content of the polyol contained in the intermittent connection part 3 is preferably 4 to 30% by mass with respect to the entire intermittent connection part 3 (the whole components constituting the intermittent connection part 3).
- the content of polyol relative to the entire intermittent connection portion 3 is less than 4% by mass, the flexibility and elongation when unitized are insufficient, and the risk of cracking of the intermittent connection portion 3 is increased when ironing is applied. There is.
- the Newton region between the low shear rate region and the high shear rate region becomes narrow, and shearing may be confirmed before reaching the high shear rate region. That is, the stability in the high shear rate region is deteriorated, which may lead to scattering of the material at the time of application.
- the content exceeds 30% by mass, the viscosity decreases, which may cause application failure or cause scattering from the roll.
- the polyol content is preferably 4 to 30% by mass with respect to the entire intermittently connected portion 3.
- UV curable resin that coats the optical fiber and components generally used as an additive component thereof can be used.
- oligomers, dilutions, and the like can be used.
- Monomers, photoinitiators, silane coupling agents, sensitizers, pigments, fillers, and other various additives can be used.
- the oligomer for example, polyether urethane acrylate, epoxy acrylate, polyester acrylate, silicone acrylate and the like can be used. These may be used alone or in combination of two or more.
- the Young's modulus and the glass transition temperature (Tg) of the intermittently connected portion 3 as a whole can be adjusted by the skeleton structure and molecular weight of the oligomer, and the type and added amount of the diluted monomer described later. As will be described later, the Young's modulus can be adjusted by reducing the molecular weight of the oligomer or increasing the functional group of the monomer.
- polyether-type urethane acrylate as an oligomer
- a polyol such as polypropylene glycol, polyethylene glycol, or polytetramethylene glycol
- a polypropylene glycol having a branched structure can be used.
- Hydroxy compound having an unsaturated double bond that is reactive to ultraviolet rays via an aromatic diisocyanate at the hydroxyl groups at both ends as a skeletal component preferably using such polypropylene glycol as an intermediate block It is preferable to use an oligomer in which is bound.
- polypropylene glycol as a polyol and using an oligomer having polypropylene glycol as an intermediate block as an oligomer, crystallization at a low temperature of ⁇ 60 ° C. does not cause crystallization, so that crystallization at a low temperature can be efficiently prevented.
- the oligomer to be used those having a weight average molecular weight of 500 to 2000 are preferred, and those having a weight average molecular weight of 1000 to 2000 are particularly preferred.
- aromatic diisocyanates such as tolylene diisocyanate (TDI) and isophorone diisocyanate (IPDI) can be used.
- TDI tolylene diisocyanate
- IPDI isophorone diisocyanate
- a hydroxy type compound such as hydroxyethyl acrylate (HEA) etc. can be used, for example.
- a dilution monomer can be blended mainly for viscosity adjustment within a range that does not interfere with the purpose and effect of adding the rheology control agent described later.
- a dilution monomer a monofunctional monomer, a bifunctional monomer, a polyfunctional monomer, etc. can be used, for example.
- dilutable monomers for example, PO-modified nonylphenol acrylate, isobornyl acrylate, 2-ethylhexyl acrylate, isononyl acrylate, isodecyl acrylate, polyethylene glycol acrylate, N-vinyl pyrrolidone, N-vinyl Examples include caprolactam and lauryl acrylate.
- Bifunctional and polyfunctional monomers include 1,6-hexanediol diacrylate, bisphenol A epoxy acrylate, tripropylene glycol diacrylate, tricyclodecane dimethylol diacrylate, EO-modified bisphenol A diacrylate, and hexanediol diacrylate.
- An acrylate etc. are mentioned. One of these may be used alone, or two or more thereof may be used in combination. Note that the monofunctional monomer has a greater effect of lowering the Young's modulus than the bifunctional monomer and the polyfunctional monomer. This is because the monofunctional monomer has a greater effect of reducing the crosslinking points in the molecular structure than the bifunctional monomer and the polyfunctional monomer.
- the photoinitiator is radicalized by absorbing ultraviolet rays, and can continuously polymerize the unsaturated double bond of the reactive oligomer and reactive monomer.
- the photoinitiator include alkylphenone photopolymerization initiators and acylphosphine oxide photopolymerization initiators such as 1-hydroxy-cyclohexyl-phenyl-ketone and 2-hydroxy-2-methyl-1-phenyl-propane- 1-one, 2,4,6-trimethylbenzoyl-diphenyl-phosphine oxide, bis (2,4,6-trimethylbenzoyl) -phenylphosphine oxide, and the like can be used. These may be used individually by 1 type, or can be used in combination of 2 or more type.
- triplet sensitizers such as thioxanthones and benzophenones are suitable, and in particular, thioxanthone has a long effect in the triplet state and can be used in combination.
- the intermittent connection part 3 which comprises the optical fiber tape core wire 2 of this invention has added the rheology control agent as a structural component.
- the rheology control agent has an effect of increasing the viscosity of the added material (in the present invention, the ultraviolet curable resin composition constituting the intermittent connection portion 3) in a low shear rate region. . Furthermore, there is an effect of reducing the inclination with respect to the temperature dependence. Furthermore, in this study, it was found that by adding a rheology control agent, shearing can be shifted to a shear rate region higher than 10 6 1 / s, which is a high shear rate region, and the coating can be stabilized.
- the rheology control agent can shift the Newton region between the low shear rate region and the high shear rate region to the high shear region side, and can impart properties such that the Newton region becomes long.
- a region in the vicinity of approximately 10 6 ( 1000000) (1 / s).
- Examples of the rheology control agent for shifting the Newton region between the low shear rate region and the high shear rate region to the high shear region side include silica such as fumed silica (also referred to as fumed silica). Inorganic fillers such as titanium oxide, calcium carbonate, heavy calcium carbonate, bentonite, and smectite, organic fillers, and the like, or liquid components can be used.
- the rheology control agent may be used alone or in combination of two or more.
- silica such as fumed silica
- fumed silica examples include hydrophobic fumed silica and hydrophilic fumed silica, and it is particularly preferable to use hydrophobic fumed silica.
- hydrophobic fumed silica when it is added to the ultraviolet curable resin composition constituting the intermittent connection portion 3, the mixing property is improved and the material is suitably dispersed.
- the material (resin composition) is satisfactorily applied to the front and back surfaces of the adjacent optical fiber colored core wires 1 and the appearance is improved.
- hydrophobic fumed silica examples include AEROSIL (registered trademark, hereinafter, the same applies to “AEROSIL”) R974 (manufactured by Nippon Aerosil Co., Ltd.).
- hydrophilic fumed silica examples include AEROSIL 200 (manufactured by Nippon Aerosil Co., Ltd.).
- the shape of the rheology control agent in the case of a solid, particles, powders, spheres, and the like can be preferably used, or liquids may be used.
- the average particle size (average primary particle size) is not particularly limited, but is preferably 0.005 ⁇ m to 10 ⁇ m, more preferably 0.007 ⁇ m to 1 ⁇ m, and 0.01 ⁇ m to 0.1 ⁇ m. It is particularly preferred. These average particle size ranges are particularly effective when hydrophobic fumed silica is used as the rheology control agent.
- the rheology control agent is used in an amount of 1 to 10% by mass with respect to the entire intermittent connection portion 3 (the entire components constituting the intermittent connection portion 3).
- the Newton region between the low shear rate region and the high shear rate region of the ultraviolet curable resin composition constituting the intermittent connection portion 3 can be adjusted. That is, with respect to the viscosity of the ultraviolet curable resin composition, the viscosity at a shear rate of 10 1 1 / s obtained from dynamic viscoelasticity at 25 ° C. (assuming a low shear rate region) is in the range of 3 to 11 Pa ⁇ s.
- the viscosity at a shear rate of 10 6 1 / s obtained from dynamic viscoelasticity at 25 ° C. (assuming a high shear rate region) can be in the range of 0.2 to 2.5 Pa ⁇ s. Compared with the case where no rheology control agent is added, the position of shearing can be shifted.
- the content of the rheology control agent is less than 1% by mass, the rheology may be insufficiently adjusted, and the viscosity may not be within the above range.
- the content exceeds 10% by mass, a coating amount when the material is applied between the optical fiber colored cores 1 by the application roll is reduced, and a problem arises that the adhesion between the optical fiber colored cores 1 decreases. There is a case.
- the viscosity at a shear rate of 10 1 1 / s obtained from dynamic viscoelasticity at 25 ° C. is in the range of 3 to 11 Pa ⁇ s
- the dynamic viscoelasticity at 25 ° C is in the range of 3 to 11 Pa ⁇ s
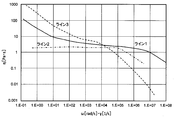
- the advantage obtained by keeping the viscosity at a shear rate of 10 6 1 / s (assuming a high shear rate region) in the range of 0.2 to 2.5 Pa ⁇ s will be described with reference to FIG.
- FIG. 6 is a diagram showing an example of the relationship between the shear rate and the viscosity.
- the vertical axis represents viscosity ⁇ (Pa ⁇ s), and the horizontal axis represents shear rate ⁇ (1 / s).
- the shear rate ⁇ (1 / s) is equivalent to the frequency ⁇ (rad / s).
- Line 1 is a curve showing the behavior of a fluid having a viscosity satisfying the requirements of the present invention with respect to the content of the polyol and the rheology control agent.
- the viscosity at a shear rate of 10 1 1 / s is maintained in the range of 3 to 11 Pa ⁇ s, and the viscosity at a shear rate of 10 6 1 / s is maintained at 0.2 to 2.5 Pa ⁇ s.
- shearing can be shifted to a shear rate region higher than 10 6 1 / s, so the Newton region becomes longer. Therefore, since the change in viscosity in the high shear rate region relative to the low shear rate region can be suppressed to a small level, it is possible to suppress the scattering of the material due to the application roll or the like and to stabilize the coating amount of the material even in the production with a high linear velocity. it can.
- the material which comprises the intermittent connection part 3 is apply
- line 2 is a case where no rheology control agent is added to the requirements of the present invention.
- shearing where the viscosity decreases at a boundary where the shear rate is lower than 10 6 (for example, 10 5 1 / s) is confirmed, and it is considered that the behavior becomes unstable in the high shear rate region.
- Line 3 is a case where, for example, no polyol is added, but the Newton region is narrow, and shearing is confirmed from a place where the shear rate is lower than 10 6 1 / s (for example, 10 4 1 / s). This is also considered to be unstable behavior in the high shear rate region. All of these are considered to be difficult to suppress scattering or the like during application of the material by the application roll.
- the viscosity from the low shear rate region to the high shear rate region of the material constituting the intermittent connection portion 3 can be measured using a commercially available viscosity measuring device (rheometer). Etc.) can be used.
- the viscosity at a shear rate of 10 1 1 / s obtained from dynamic viscoelasticity at 25 ° C. is obtained from the dynamic viscoelasticity at 25 ° C. within the range of 5 to 11 Pa ⁇ s.
- the viscosity at a shear rate of 10 6 1 / s is more preferably in the range of 0.4 to 2.4 Pa ⁇ s.
- the viscosity ratio (25 ° C. viscosity / 35 ° C. viscosity) is particularly preferably 2 or less. .
- the viscosity at a shear rate of 10 1 1 / s determined from dynamic viscoelasticity at 35 ° C. is preferably in the range of 1.5 to 6 Pa ⁇ s.
- the adhesive strength between the optical fiber colored core wire 1 and the intermittent connection part 3 is 0.07 N or more. As long as the adhesive strength is within a range, the above-described effects are efficiently exhibited, and the optical fiber colored core wire 1 and the intermittent connection portion 3 are appropriately bonded (adhered).
- the adhesive strength is more preferably 0.07 to 0.25N, further preferably 0.07 to 0.20N, and particularly preferably 0.07 to 0.15N. As long as the adhesive strength is within the range, the optical fiber colored core wire 1 and the intermittent connection portion 3 are appropriately bonded (contacted), and the separation (working) property of the optical fiber colored core wire 1 can be maintained. .
- the amount of resin applied to the intermittent connection portion 3 is controlled by the resin pressure at the time of manufacture (the same as the application pressure; the same shall apply hereinafter), and adhesion is performed as the resin amount of the intermittent connection portion 3 decreases (adhesion surface becomes smaller).
- the strength is reduced, if the resin is applied so as to be higher than the colored optical fiber 1, the optical fiber adjacent to the optical fiber 2 is folded when the optical fiber ribbon 2 is folded and densified into a cable. There may be a problem that the tape core wire 2 hits to cause macrobending (increase in transmission loss) or the intermittent connection portion 3 is broken.
- the adhesive strength is excessively high, separation (working) property cannot be ensured, so that the resin constituting the intermittent connection portion 3 is applied to the extent that the height between the two optical fiber colored cores 1 is not exceeded. This is preferable because macrobending can be suppressed.
- Bond strength and separability (working) are often influenced by the length of the interface (length of the bonded portion) where one optical fiber colored core wire 1 and the intermittently connected portion 3 are in contact.
- the length of the bonded portion is appropriately determined depending on the material constituting the intermittent connecting portion 3, the shape of the intermittent connecting portion 3, and the like, but is preferably about 5 to 35 mm, and the length of the bonded portion is within such a range. As a result, both good adhesive strength and separation (working) properties are secured.
- the type or the like of the material is appropriately selected by using the materials described above or later as the intermittent connection portion 3. Then, it is carried out by adjusting the resin pressure of the resin, the length of the bonded portion, the ultraviolet curing conditions such as the irradiation amount, and the like.
- the adhesive strength between the optical fiber colored core wire 1 and the intermittent connection portion 3 can be measured, for example, as follows.
- the two optical fiber colored cores 1 formed with the intermittent connection part 3 are taken out, and the optical fiber colored cores 1 are fixed to the upper part of the tensile tester, and ⁇ 0 is placed between the two optical fiber colored cores 1.
- the resin material (ultraviolet curable resin composition) constituting the intermittent connection portion 3 includes the following additives, for example, light stabilizers such as antioxidants, ultraviolet absorbers, hindered amine light stabilizers, Deterioration inhibitors such as thermal polymerization inhibitors, silane coupling agents, leveling agents, hydrogen absorbers, chain transfer agents, silicones, lubricants, etc. may be added as necessary within the range that does not interfere with the purpose and effect of the present invention. it can.
- light stabilizers such as antioxidants, ultraviolet absorbers, hindered amine light stabilizers
- Deterioration inhibitors such as thermal polymerization inhibitors, silane coupling agents, leveling agents, hydrogen absorbers, chain transfer agents, silicones, lubricants, etc. may be added as necessary within the range that does not interfere with the purpose and effect of the present invention. it can.
- the intermittent connection part 3 may be colored.
- the pigment that is added when coloring the intermittent connection portion 3 include organic pigments such as phthalocyanine, quinacridone, dioxan, and Bensui imidazolone, and inorganic pigments such as carbon black and titanium oxide.
- the content of the colorant may be appropriately determined depending on the material constituting the intermittent connection part 3, the content of the pigment contained in the colorant, the type of other components such as an ultraviolet curable resin, and the like.
- the content is preferably 0.5 to 3.0% by mass, particularly preferably 1.5 to 2.5% by mass with respect to the whole.
- adhesion confirmation of the intermittent connection part 3 and the optical fiber tape core 2 can be performed continuously in a production line. .
- the material include the ultraviolet curable resin and its additives listed as the components constituting the intermittent connection part 3 described above, for example, oligomer, dilution monomer, photoinitiator, silane coupling agent, sensitizer, pigment (and Components such as the above-mentioned various additives such as a coloring material obtained by mixing a pigment and an ultraviolet curable resin, a lubricant, and the like can be preferably used.
- the oligomer for example, as the primary coating layer 11 and the secondary coating layer 12, aromatic isocyanate and hydroxyethyl acrylate are added to a polyol using polypropylene glycol, which is the same as that constituting the intermittent connection portion 3 described above. It is preferable to use the above oligomer, and the Young's modulus can be adjusted by changing the molecular weight of the polyol (polypropylene glycol) in the intermediate block.
- the weight average molecular weight of the oligomer used is preferably 1000 to 4000 when used as the primary coating layer 11, and 500 to 2000 when used as the secondary coating layer 12. It is preferable to use 500 to 2000 when used as the colored layer 13, and 500 to 2000 when used as the colored secondary coating layer 12a. Is preferred.
- the primary coating layer 11 and the secondary coating layer 12 are not crystallized even at a low temperature of ⁇ 60 ° C. by using polypropylene glycol as a polyol and an oligomer having polypropylene glycol as an intermediate block as an oligomer. Therefore, crystallization at low temperatures can be efficiently prevented.
- aromatic isocyanate for example, aromatic diisocyanates such as tolylene diisocyanate (TDI) and isophorone diisocyanate (IPDI) can be used.
- TDI tolylene diisocyanate
- IPDI isophorone diisocyanate
- HOA hydroxyethyl acrylate
- a dilution monomer can be blended mainly for viscosity adjustment.
- a monofunctional monomer for example, PO-modified nonylphenol acrylate, isobornyl acrylate, 2-ethylhexyl acrylate, isononyl acrylate, isodecyl acrylate, polyethylene glycol acrylate, N-vinyl pyrrolidone, N-vinyl Examples include caprolactam.
- bifunctional monomer and polyfunctional monomer examples include 1,6-hexanediol diacrylate, bisphenol A epoxy acrylate, tripropylene glycol diacrylate, tricyclodecane dimethylol diacrylate, and the like. One of these may be used alone, or two or more thereof may be used in combination.
- the monofunctional monomer has a greater effect of lowering the Young's modulus than the bifunctional monomer and the polyfunctional monomer. This is because the monofunctional monomer has a greater effect of reducing the crosslinking points in the molecular structure than the bifunctional monomer and the polyfunctional monomer.
- the photoinitiator absorbs ultraviolet rays, the photoinitiator is radicalized, and the unsaturated double bond of the reactive oligomer and the reactive monomer can be continuously polymerized.
- the photoinitiator for example, an alkylphenone photopolymerization initiator or an acyl phosphine oxide photopolymerization initiator can be used. These may be used individually by 1 type, or can be used in combination of 2 or more type.
- the oligomer which comprises the colored layer 13 the oligomer which added the aromatic isocyanate and hydroxyethyl acrylate to the polyol which uses polypropylene glycol similarly to the above-mentioned primary coating layer 11 and the secondary coating layer 12 is used. It is preferable that the Young's modulus can be adjusted by changing the molecular weight of the polyol (polypropylene glycol) in the intermediate block, or by using a bifunctional monomer or a polyfunctional monomer.
- urethane acrylate or hydroxypivalic acid neopentyl glycol acrylic acid adduct can be used as the resin constituting the colored layer 13, and in addition, bisphenol A epoxy acrylate or the like can be added to make the resin strong. Can raise the sex.
- the colored secondary coating layer 12a also serves as the colored layer 13
- the colored secondary coating layer 12a may be used as these components.
- the oligomer it is preferable to use an oligomer obtained by adding aromatic isocyanate and hydroxyethyl acrylate to a polyol using polypropylene glycol, and changing the molecular weight of the middle block polyol (polypropylene glycol)
- the Young's modulus can be adjusted by using a bifunctional monomer or a polyfunctional monomer.
- a bifunctional monomer or a polyfunctional monomer for example, by adding bisphenol A epoxy acrylate or the like as an oligomer, toughness can be increased, and further, urethane acrylate or hydroxypivalate neopentyl glycol acrylic acid adduct can be used.
- a both-end-type acrylic-modified silicone, one-end-type acrylic-modified silicone, a side-chain-end acrylic-modified silicone, or the like can be used.
- the photoinitiator include 2-methyl-1- (4-methylthiophenyl) -2-morpholinopropan-1-one, 2-benzyl-2-dimethylamino-1- (4-morpholinophenyl)- Butanone-1,2,4-diethylthioxanthone, 2,4,6-trimethylbenzoyl-diphenyl-phosphine oxide, 1-hydroxy-cyclohexyl-phenyl-ketone and the like can be used.
- each layer in the optical fiber colored core wire 1 is generally 80 ⁇ m to 125 ⁇ m and the outer diameter of the primary coating layer 11 in order to maintain the characteristics as an optical fiber (see below). Is preferably 120 ⁇ m to 200 ⁇ m, the outer diameter of the secondary coating layer 12 is 160 ⁇ m to 242 ⁇ m, and the outer diameter of the colored layer 13 is preferably 173 ⁇ m to 255 ⁇ m. As shown in FIG. 2, when the secondary coating layer 12 also serves as the colored layer 13, the colored secondary coating layer 12a preferably has an outer diameter in the range of 160 ⁇ m to 255 ⁇ m. .
- (V) Manufacturing method of optical fiber ribbon 2 An example of the manufacturing method of the optical fiber ribbon 2 according to the present invention will be described.
- the glass optical fiber 10 will be described as an example of the optical fiber 10
- an optical fiber made of quartz glass (glass optical fiber 10) coated with the primary coating layer 11 and the secondary coating layer 12 will be described as an optical fiber. It is called a strand.
- the optical fiber colored core wire 1 In order to manufacture the optical fiber colored core wire 1, for example, first, a preform mainly composed of quartz glass is heated and melted in a drawing furnace to obtain a quartz glass optical fiber (glass optical fiber 10). Next, a component containing a liquid ultraviolet curable resin is applied to the glass optical fiber 10 using a coating die, and then ultraviolet rays are applied to the component containing the ultraviolet curable resin applied by the ultraviolet irradiation device (UV irradiation device). Irradiate to cure such components. In this way, an optical fiber strand in which the glass optical fiber 10 is coated with the primary coating layer 11 and the secondary coating layer 12 is manufactured. Immediately after drawing, the outer periphery of the glass optical fiber 10 is immediately coated with a component containing an ultraviolet curable resin to form the primary coating layer 11 and the secondary coating layer 12, thereby preventing a reduction in strength of the obtained optical fiber. Can do.
- UV irradiation device ultraviolet irradiation device
- the optical fiber colored core wire 1 is manufactured by covering the outer periphery of the obtained optical fiber with the colored layer 13.
- the secondary coating layer 12 may be colored to form the optical fiber colored core wire 1 as the secondary coating layer 12a in which the outermost layer is colored.
- the optical fiber colored cores 1 obtained are arranged in a desired number, the material constituting the intermittent connection part 3 is applied in a predetermined pattern, and cured under predetermined conditions to form the intermittent connection part 3.
- the optical fiber ribbon 2 can be obtained.
- the optical fiber ribbon 2 can be manufactured, for example, by aligning a plurality of optical fiber colored cores 1 in parallel and by intermittently applying the constituent material of the intermittent connection portion 3 to a part of the outer periphery. It can be carried out using a production apparatus provided with a coating roll 6 (see FIG. 7 and the like to be described later). For example, it can be carried out using a production apparatus and a production method disclosed in Japanese Patent No. 6169060. it can.
- a plurality of optical fiber colored cores 1 are brought into contact with the respective application rolls, and the constituent material of the intermittent connection portion 3 is intermittently applied to the side surfaces of the optical fiber colored cores 1, while the alignment means By aligning the side surfaces of the optical fiber colored core wire 1 coated with the material constituting the intermittent connection portion 3 on the side surfaces so as to contact each other, and curing the above-described constituent materials by ultraviolet irradiation or the like, the intermittent connection portion 3 What is necessary is just to connect the optical fiber colored core wires 1 intermittently and to obtain the optical fiber tape core wire 2.
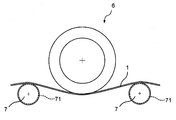
- FIG. 7 is a view showing an example of the application roll 6.
- the application roll 6 shown in FIG. 7 adopts a configuration in which the application roll 6 is sandwiched between a pair of V-groove rolls 7 in which V-grooves 71 are formed. 1 will come into contact.
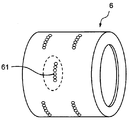
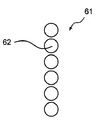
- FIG. 8 is a perspective view showing another example of the coating roll 6, and FIG. 9 is an enlarged view of the coating hole 61 formed in the coating roll 6 of FIG.
- the application roll 6 shown in FIG. 8 is provided with the application hole 61 shown in FIG. 9, and the application hole 61 is not a single continuous long hole, but a plurality of small holes 62 arranged in a line. Composed. That is, the coating hole 61 is formed by continuously arranging a plurality of small holes 62 with a predetermined width and a predetermined length.
- the coating hole 61 having such a configuration By using the coating hole 61 having such a configuration, the extrusion amount of the material (ultraviolet curable resin) R constituting the intermittent connection portion is stabilized. Since each small hole 62 is independent in the application hole 61, a substantially constant material R is extruded from each small hole 62. Therefore, since a substantially constant amount of material R can be pushed out to the coating hole 61 (the range where the small holes 62 are formed), the amount of the material R applied to the optical fiber colored core wire 1 is stabilized. .
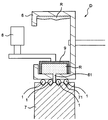
- FIG. 10 is a cross-sectional view showing the device D in the vicinity of the coating roll 6.
- the apparatus D shown in FIG. 10 employs a configuration in which the die 9 is pressed with a predetermined load in the vicinity of the coating roll 6 in the extrusion direction of the material R, and air is used as a member for holding the die 9.
- a cylinder 8 is provided.
- the die 9 is pressed by the air cylinder 8 with a constant load toward the application side of the material R to the optical fiber colored core wire 1 that is in contact with the V groove 71 of the V groove roll 7.
- the material R is applied from the application hole 61.
- an elastic member such as a spring may be provided.
- the optical fiber ribbon 2 according to the present invention described above contains a polyol having a weight average molecular weight of 2500 to 4000 with respect to the material (ultraviolet curable resin composition) constituting the intermittent connection portion 3, Contains a rheology control agent in a specific range.
- the material constituting the intermittent connection portion 3 has a relatively high viscosity in the low shear rate region and a relatively low viscosity in the high shear rate region, while being in the high shear rate region.
- optical fiber cable 4 provided with the optical fiber ribbon 2 according to the present invention enjoys the effect of the optical fiber ribbon 2 described above. That is, the scattering of the material by the coating roll 6 etc. at the time of manufacture of the intermittent connection part 3 can be suppressed, the coating amount to the optical fiber colored core wire 1 can be stabilized, and the line speed can be increased to suppress such scattering.
- An optical fiber cable 4 having an optical fiber ribbon 2 that can be maintained even during manufacture is provided.
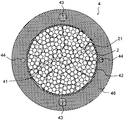
- FIG. 11 is a diagram showing an aspect of the optical fiber cable 4.
- a predetermined number (25 in FIG. 11) of optical fiber units 21 obtained by twisting or bundling a predetermined number (8 in FIG. 11) of optical fiber tape cores 2 having a predetermined number of cores are twisted or bundled.
- the cable core 41 is configured.
- a buffer layer 42 made of, for example, a non-woven presser tape or the like is formed around the cable core 41.
- two steel wires (tension members) 43 and two tear strings 44 are formed around the buffer layer 42.
- a covering layer (sheath) 46 made of a thermoplastic resin or the like is formed.
- FIG. 12 is a diagram showing another aspect of the optical fiber cable 4.
- the optical fiber cable 4 in FIG. 12 has a predetermined number of optical fiber units 21 formed by twisting or bundling a predetermined number of optical fiber ribbons 2 (not shown in FIG. 12) with a predetermined number of cores. (Eight in FIG. 12)
- the loose tube 5 is built in a twisted or bundled state, and the optical fiber unit 21 and the loose tube 5 containing the optical fiber unit 21 are arranged around a steel wire (tension member) 43 in a predetermined number. (8 in FIG. 12) Twist together.
- a buffer layer 42 made of, for example, a non-woven presser tape or the like is formed around the periphery, and a predetermined number (15 in FIG. 12) of optical fiber units 21 and the loose tubes 5 incorporating the optical fiber units 21 are provided around the buffer layer 42. ) Arrange and twist.
- a buffer layer 42 made of, for example, a non-woven presser tape and a coating layer (sheath) 46 made of a thermoplastic resin are formed around the periphery.
- the optical fiber cable 4 may be an optical fiber cable such as a center tube type, a loose tube type, or a slot type, and is not particularly limited as long as the optical fiber cable accommodates the optical fiber ribbon 2.
- the coating layer 46 can be, for example, 2.0 to 3.0 mm, but is not particularly limited to this range.
- the configuration of the 12 fibers shown in FIGS. 3 to 5 has been described as an example of the optical fiber ribbon 2, but the number of cores in the optical fiber ribbon 2 (optical fiber coloring) is described.
- the number of cores 1) can be arbitrarily determined in addition to 12 cores, such as 4 cores, 8 cores, and 24 cores.
- the cross-sectional shape of the intermittent connection part 3 although the 2 sides which contact
- the relationship between the shear rate and the viscosity shown in FIG. 6 is merely an example.
- the line 1 using the component having the requirements of the present invention as the constituent material of the intermittent coupling portion 3 also has the requirements of the present invention.
- the structure shown in FIGS. 11 and 12 is described as an example of the optical fiber cable 4 including the optical fiber ribbon 2, but the structure of the optical fiber cable 4 is the above-described structure.
- the type and thickness of the coating layer 46, the number and size of the optical fiber colored core wire 1 and the optical fiber tape core wire 2, the number and size of the optical fiber units 21, and the optical fiber The number of optical fiber ribbons 2 in the unit 21, the type, number and size of steel wires (tension members) 43, the type and thickness of the buffer layer 42, and the number of layers can be freely selected. .
- the outer diameter, cross-sectional shape, etc. of the optical fiber cable 4 can be freely selected.
- the specific structure, shape, and the like in the implementation of the present invention may be other structures as long as the object of the present invention can be achieved.
- optical fiber colored core wires shown in FIGS. 1 and 2 were provided by the methods shown in (1) and (2) below, as shown in FIGS.
- An optical fiber ribbon having the configuration shown in FIG. 5 was manufactured.
- the molecular weight refers to “weight average molecular weight”.
- the following component was used about the primary coating layer, the secondary coating layer, the colored layer, and the intermittent connection part.
- optical fiber colored core Around an optical fiber made of quartz glass and having an outer diameter of 125 ⁇ m, the outer diameter of the primary coating layer (primary layer) is 195 ⁇ m and the outer diameter of the secondary coating layer (secondary layer) is 242 ⁇ m. The layer was coated into an optical fiber. The obtained optical fiber is coated with a colored layer (the component that becomes the colored layer is component a) around the secondary coating layer in a separate process. An optical fiber colored core wire having a diameter of 255 ⁇ m was obtained.
- optical fiber colored core Around a glass optical fiber made of quartz glass having an outer diameter of 125 ⁇ m, which is an optical fiber, an outer diameter of the primary coating layer (primary layer) is 185 ⁇ m, and a colored secondary coating layer (with a colored secondary coating layer and The component is component b.) The outer diameter was 255 ⁇ m and each layer was coated to obtain an optical fiber colored core wire having an outer diameter of 255 ⁇ m having the configuration shown in FIG.
- the primary coating layer and the secondary coating layer are made of an oligomer using polypropylene glycol as an ultraviolet curable resin (polypropylene glycol as an intermediate block, and skeleton component having hydroxyethyl acrylate as a skeleton component via tolylene diisocyanate. Oligomer)), dilutable monomer, photoinitiator, and additives were mixed and used in appropriate amounts.
- Component a optical fiber colored core wire as shown in FIG. 1:
- the UV curable resin constituting component a (colorant component a) to be a colored layer uses urethane acrylate or bisphenol A epoxy acrylate as an oligomer, and a Young's modulus by adding a bifunctional monomer or a polyfunctional monomer as a monomer. Adjusted. Moreover, 3 mass% of both terminal type acrylic modified silicone was contained with respect to the whole colored layer.
- Photoinitiators are 2-methyl-1- (4-methylthiophenyl) -2-morpholinopropan-1-one (Irgacure 907), 2,4,6-trimethylbenzoyl-diphenyl-phosphine oxide (lucillin TPO), 2,4-Diethylthioxanthone (Kayacure DETX-S) was added.
- the oxygen concentration in the production was adjusted to 3 to 5%, and the ultraviolet irradiation amount was 80 mJ / cm 2 or less.
- Component b optical fiber colored core wire as shown in FIG. 2:
- the ultraviolet curable resin constituting component b (coloring material component b) to be a colored secondary coating layer (colored layer) is obtained by adding aromatic isocyanate and hydroxyethyl acrylate to a polyol using polypropylene glycol as an oligomer.
- the Young's modulus was adjusted by changing the molecular weight of the middle block polyol (polypropylene glycol) or by using a bifunctional monomer or a polyfunctional monomer.
- the viscosity of the material constituting the intermittent connection portion was confirmed by the following method, and the presence or absence of material scattering in the application of the material constituting the intermittent connection portion was confirmed.
- blending degree (mixability) of the rheology control agent with respect to a base material and the external appearance of the intermittent connection part were also confirmed for reference. The results are shown in Table 1 together with the composition.
- Base material used as a component of intermittent connection Oligomer as an ultraviolet curable resin (an oligomer in which a polypropylene glycol having a weight average molecular weight of 2000 is used as an intermediate block and hydroxyethyl acrylate is bonded to hydroxyl groups at both ends as a skeleton component via tolylene diisocyanate). Isobornyl acrylate and PO-modified nonylphenol acrylate were used as monofunctional monomers, and tricyclodecane dimethylol diacrylate and 1,6-hexanediol diacrylate were used as bifunctional monomers.
- photoinitiators 1-hydroxy-cyclohexyl-phenyl-ketone, 2,4,6-trimethylbenzoyl-diphenyl-phosphine oxide was used. Further, a suitable amount of hindered amine light stabilizer and silicone (weight average molecular weight: about 10,000) as light stabilizers were mixed as additives. A material composed of these components is used as a base material, and a polyol (rheology control agent composition) is formed as a material (ultraviolet curable resin composition) by adding a polyol and a rheology control agent shown below at a predetermined content. In Comparative Example 1, a polyol is added, and in Comparative Example 2, only a rheology control agent is added.)
- Example 1 Polypropylene glycol having a weight average molecular weight of 3000 as a polyol (PP3000: manufactured by Sanyo Chemical Industries, Ltd.) is used as the base material, and an ultraviolet curable resin composition (a material constituting the intermittent connection portion). In some cases.) 23 mass% of the total was added. Moreover, 5 mass% of hydrophobic fumed silica (AEROSIL R974: Nippon Aerosil Co., Ltd.) was added as a rheology control agent with respect to the whole composition.
- PP3000 manufactured by Sanyo Chemical Industries, Ltd.
- Example 2 Polypropylene glycol having a weight average molecular weight of 3000 (PP3000: manufactured by Sanyo Chemical Industries, Ltd.) as a polyol was added to the base material in an amount of 23% by mass based on the entire composition. Moreover, 4 mass% of hydrophobic fumed silica (AEROSIL R974: Nippon Aerosil Co., Ltd. product) was added as a rheology control agent with respect to the whole composition.
- PP3000 manufactured by Sanyo Chemical Industries, Ltd.
- AEROSIL R974 Nippon Aerosil Co., Ltd. product
- Example 3 25 mass% of polypropylene glycol having a weight average molecular weight of 3000 (PP3000: manufactured by Sanyo Chemical Industries, Ltd.) as a polyol was added to the base material. Moreover, 6 mass% of hydrophobic fumed silica (AEROSIL R974: Nippon Aerosil Co., Ltd.) was added as a rheology control agent with respect to the whole composition.
- PP3000 weight average molecular weight of 3000
- AEROSIL R974 Nippon Aerosil Co., Ltd.
- Example 4 Polypropylene glycol having a weight average molecular weight of 3000 (PP3000: manufactured by Sanyo Chemical Industries, Ltd.) as a polyol was added to the base material in an amount of 20% by mass based on the entire composition. Moreover, 5 mass% of hydrophobic fumed silica (AEROSIL R974: Nippon Aerosil Co., Ltd.) was added as a rheology control agent with respect to the whole composition.
- PP3000 manufactured by Sanyo Chemical Industries, Ltd.
- AEROSIL R974 Nippon Aerosil Co., Ltd.
- Example 5 Polypropylene glycol having a weight average molecular weight of 3000 (PP3000: manufactured by Sanyo Chemical Industries, Ltd.) as a polyol was added to the base material in an amount of 4% by mass based on the entire composition. Moreover, 1 mass% of hydrophobic fumed silica (AEROSIL R974: Nippon Aerosil Co., Ltd. product) was added as a rheology control agent with respect to the whole composition.
- PP3000 manufactured by Sanyo Chemical Industries, Ltd.
- Example 6 Polypropylene glycol having a weight average molecular weight of 3000 (PP3000: manufactured by Sanyo Chemical Industries, Ltd.) as a polyol was added to the base material by 30% by mass with respect to the entire composition. Moreover, 10 mass% of hydrophobic fumed silica (AEROSIL R974: Nippon Aerosil Co., Ltd.) was added as a rheology control agent with respect to the whole composition.
- PP3000 manufactured by Sanyo Chemical Industries, Ltd.
- AEROSIL R974 Nippon Aerosil Co., Ltd.
- Example 7 Polypropylene glycol having a weight average molecular weight of 3000 (PP3000: manufactured by Sanyo Chemical Industries, Ltd.) as a polyol was added to the base material in an amount of 23% by mass based on the entire composition. Moreover, 5 mass% of hydrophilic fumed silica (AEROSIL 200: Nippon Aerosil Co., Ltd. product) was added as a rheology control agent with respect to the whole composition.
- PP3000 manufactured by Sanyo Chemical Industries, Ltd.
- Viscosity measurement method and viscosity calculation method, etc. Using a rheometer (MCR301: Anton Paar), the viscosity from the low shear rate region to the high shear rate region was measured. 25 ⁇ parallel plate, gap 0.5 mm, frequency 62.8 to 0.68 rad / s (10 to 0.1 Hz, log 4 points / digit, 9 points in total), strain 5%, temperature ⁇ 50 ° C. to 50 ° C. (10 ° C. Frequency dispersion (relationship between frequency and viscosity) was obtained under the condition of ticks.
- the reference temperature is 25 ° C. where the material constituting the intermittent connection portion is applied.
- L Using the F (Williams, Landel, Ferry) formula, a shift factor Log ⁇ T indicating the relationship between the horizontal movement amount and the temperature change was defined, and the master curve shown in FIG. 13 was obtained.
- FIG. 14 is a graph showing the relationship between the shear rate and the viscosity.
- Example 1, Comparative Example 1, and Comparative Example 2 are listed as representative examples.
- Table 1 as the viscosity (Pa ⁇ s), (x) the viscosity at a shear rate of 10 1 1 / s determined from dynamic viscoelasticity at 25 ° C. (viscosity 25 ° C.
- Viscosity at a shear rate of 10 6 1 / s determined from dynamic viscoelasticity at 25 ° C. (viscosity 25 ° C. 10 ⁇ 6 1 / s), (z) Shear rate determined from dynamic viscoelasticity at 35 ° C. Viscosity of 10 1 1 / s (viscosity 35 ° C. 10 ⁇ 1 1 / s), and viscosity ratio (rounded to the first decimal place) (viscosity 25 ° C. 10 ⁇ 1 1 / s) / (viscosity 35 °C 10 ⁇ 1 1 / s) ( (x) / (z)).
- Table 1 shows the measurement results of the viscosity.
- Examples 1 to 7 as a result of measuring the viscosity of the material constituting the intermittently connected portion (the UV curable resin composition to be applied), all have shear rates of 10 1 determined from dynamic viscoelasticity at 25 ° C.
- the viscosity at 1 / s was in the range of 3 to 11 Pa ⁇ s, and the viscosity at a shear rate of 10 6 1 / s determined from dynamic viscoelasticity at 25 ° C. was in the range of 0.2 to 2.5 Pa ⁇ s. It was.
- Example 1 the Newton region became longer, the shearing shifted after 10 6 1 / s, and the viscosity change (decrease in viscosity) in the high shear region was small. Therefore, in the evaluation of the material scattering confirmation, the material scattering was not confirmed even when the linear velocity was 400 m / min or 600 m / min, which was effective in preventing the scattering.
- Example 2 containing a predetermined amount of the rheology control agent but not containing polyol, the Newton region is narrower than that of Example 1 described above, and shearing is observed from 10 4 1 / s as shown in FIG. Therefore, it was not stable in the high shear rate region.
- the material scattering was confirmed when the linear velocity was 200 m / min.
- the measurement results of the adhesive strength are also shown in Table 1.
- Examples 1 to 5 as a result of measuring the adhesive strength of the material constituting the intermittently connected portion of the optical fiber colored core wire (the UV curable resin composition to be applied), production of a high linear velocity (600 m / min) was performed. However, a high adhesive strength of 0.07N or more was obtained.
- Comparative Examples 1 to 3 do not follow the linear velocity, so that it is difficult to produce a satisfactory optical fiber ribbon, and the bonded portion is measured, but the adhesive strength is low (0.07 N). (Lower) results were confirmed.
- optical fiber cable 18 (or 36) optical fiber units in which 8 pieces of 12 optical fiber ribbons were twisted were twisted to form a cable core, and a nonwoven fabric holding tape was wound around it as a buffer layer. Furthermore, a coating layer was formed on the outer periphery of the buffer layer together with FRP of ⁇ 4 mm, two steel wires, and two tear strings. For cable formation, a thermoplastic resin was coated as a covering layer (sheath) to form a cable having the structure shown in FIG. 11 (the number of optical fiber units is different).
- the optical fiber ribbon of the present invention could be cabled in the same manner as a conventional optical fiber ribbon and could be suitably used as an optical fiber cable.
- the present invention can be effectively used as a means for providing an optical fiber ribbon and an optical fiber cable that can prevent scattering of the material constituting the intermittent connection portion during manufacturing, and has high industrial applicability.
- Optical fiber colored core wire 10 ...
- Optical fiber (glass optical fiber) 11 Primary coating layer (primary layer) 12 ; Secondary coating layer (secondary layer) 12a: Colored secondary coating layer 13: Colored layer 2:
- Optical fiber tape core wire 21 Optical fiber unit 3: Intermittent connection part 31, 32: Intermittent connection part 33, X: Non-connection Part (single core) 4 ...
Landscapes
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- Optics & Photonics (AREA)
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Optical Fibers, Optical Fiber Cores, And Optical Fiber Bundles (AREA)
Abstract
Description
まず、光ファイバテープ心線2を構成する光ファイバ着色心線1の一態様を説明する。図1は、光ファイバ着色心線1の構造の一例を示した断面図である。また、図2は、光ファイバ着色心線1の構造の他の例を示した断面図である。図1及び図2中、1は光ファイバ着色心線、10は光ファイバ、11は一次被覆層、12は二次被覆層、12aは着色された二次被覆層(図2のみ)、13は着色層(図1のみ)、をそれぞれ示す。
図3は、光ファイバテープ心線2の一態様を示した正面図である。図4及び図5は、光ファイバテープ心線2の連結状態を示した図(図4は間欠連結部31を含む図3のA-A断面図、図5は間欠連結部32を含む図3のB-B断面図である。)である。なお、図3ないし図5では、便宜的に、12心の光ファイバ着色心線1から構成される光ファイバテープ心線2を示している。
前記した図3等に示した間欠連結部3は、例えば、下記の成分を硬化させて形成することができる。本発明において、間欠連結部3を構成する成分としては、重量平均分子量(Mw)が2500~4000のポリオールを含有する。かかる重量平均分子量(以下、単に「分子量」とすることもある。)のポリオールは、間欠連結部3を構成する紫外線硬化樹脂の網目に反応しないで存在することができる。間欠連結部3は、紫外線硬化樹脂の稠密な網目構造にポリオールが膨潤していることになり、紫外線硬化樹脂に対して可塑剤的な役割を果たす。これにより、間欠連結部3のヤング率を適度にさせるとともに、低温条件下でも間欠連結部3にしなやかさ及び伸びを付与することができる。また、ポリオールは、間欠連結部3の表面にブリードして、光ファイバユニット21同士の摩擦を抑えることができる。
本発明に係る光ファイバ着色心線1の一次被覆層11(プライマリ層)及び二次被覆層12(セカンダリ層)の構成材料となる樹脂材料や、光ファイバ着色心線1の着色層13の構成材料としては、前記した間欠連結部3を構成する成分として挙げた紫外線硬化樹脂及びその添加剤である、例えば、オリゴマー、希釈モノマー、光開始剤、シランカップリング剤、増感剤、顔料(及び顔料と紫外線硬化樹脂等を混合した着色材)、滑剤等、前記した各種の添加剤等の成分を好ましく使用することができる。
本発明に係る光ファイバテープ心線2の製造方法の一例を説明する。なお、以下において、光ファイバ10としてガラス光ファイバ10を例に挙げて説明し、一次被覆層11と二次被覆層12とが被覆された石英ガラス製光ファイバ(ガラス光ファイバ10)を光ファイバ素線とよんでいる。
以上説明した本発明に係る光ファイバテープ心線2は、間欠連結部3を構成する材料(紫外線硬化樹脂組成物)に対して、重量平均分子量が2500~4000のポリオールを含有することに加え、レオロジーコントロール剤を特定の範囲で含有している。かかる構成により、間欠連結部3を構成する材料が、当該材料に対して低せん断速度域では比較的高粘度となり、高せん断速度域では比較的低粘度となる一方、高せん断速度域である106 1/sより高いせん断速度域にシアシニングをシフトし、ニュートン域が長くなるような性質を備え、製造時に当該材料を塗布する塗布ロール6等の回転に伴い生ずる遠心力により材料の飛散を抑え、光ファイバ着色心線1への塗布量を安定させることができる。かつ、かかる飛散の抑制等を、線速を高速とした製造でも維持することができる光ファイバテープ心線2となる。
なお、以上説明した態様は、本発明の一態様を示したものであって、本発明は、前記した実施形態に限定されるものではなく、本発明の構成を備え、目的及び効果を達成できる範囲内での変形や改良が、本発明の内容に含まれるものであることはいうまでもない。また、本発明を実施する際における具体的な構造及び形状等は、本発明の目的及び効果を達成できる範囲内において、他の構造や形状等としても問題はない。本発明は前記した各実施形態に限定されるものではなく、本発明の目的を達成できる範囲での変形や改良は、本発明に含まれるものである。
その他、本発明の実施の際の具体的な構造及び形状等は、本発明の目的を達成できる範囲で他の構造等としてもよい。
表1に示した内容及び下記に示した成分を用いて、下記(1)、(2)に示した方法により、図1及び図2に示した光ファイバ着色心線を備えた、図3ないし図5に示した構成の光ファイバテープ心線を製造した。なお、下記の内容において、分子量とは「重量平均分子量」を指す。なお、一次被覆層、二次被覆層、着色層及び間欠連結部については、下記の成分を使用した。
光ファイバである、石英ガラスからなる外径が125μmのガラス光ファイバの周囲に、一次被覆層(プライマリ層)の外径を195μm、二次被覆層(セカンダリ層)の外径を242μmとしてそれぞれの層を被覆して光ファイバ素線とした。得られた光ファイバ素線に対して、別工程にて二次被覆層の周囲に着色層(着色層となる成分は成分aとした。)を被覆して、図1に示した構成の外径255μmの光ファイバ着色心線を得た。
光ファイバである、石英ガラスからなる外径が125μmのガラス光ファイバの周囲に、一次被覆層(プライマリ層)の外径を185μm、着色された二次被覆層(着色された二次被覆層となる成分は成分bとした。)の外径を255μmとしてそれぞれの層を被覆して、図2に示した構成の外径255μmの光ファイバ着色心線を得た。
一次被覆層及び二次被覆層は、紫外線硬化樹脂としてポリプロピレングリコールを使用したオリゴマー(ポリプロピレングリコールを中間ブロックとし、骨格成分として、その両末端の水酸基に、トリレンジイソシアネートを介して、ヒドロキシエチルアクリレートを結合させたオリゴマーのこと。)、希釈性モノマー、光開始剤、添加剤を適当量混合して使用した。
着色層となる成分a(着色材成分a)を構成する紫外線硬化樹脂は、オリゴマーとしてはウレタンアクリレートやビスフェノールAエポキシアクリレートを使用し、モノマーとして二官能モノマーや多官能モノマーを添加することでヤング率を調整した。また、両末端型アクリル変性シリコーンを着色層全体に対して3質量%含有させた。光開始剤は、2-メチル-1-(4-メチルチオフェニル)-2-モルフォリノプロパン-1-オン(Irgacure907)、2,4,6-トリメチルベンゾイル-ジフェニル-フォスフィンオキサイド(ルシリンTPO)、2,4-ジエチルチオキサントン(カヤキュアーDETX-S)を添加した。製造における酸素濃度は3~5%で調整し、紫外線照射量は80mJ/cm2以下とした。
着色された二次被覆層(着色層)となる成分b(着色材成分b)を構成する紫外線硬化樹脂は、オリゴマーとして、ポリプロピレングリコールを使用したポリオールに芳香族系イソシアネートとヒドロキシエチルアクリレートを付加したオリゴマーを使用し、中間ブロックのポリオール(ポリプロピレングリコール)の分子量を変化させることや、二官能モノマーや多官能モノマーを使用することでヤング率を調整した。また、強靱性の向上のため、ビスフェノールAエポキシアクリレートを添加し、また、側鎖端アクリル変性シリコーンを着色層全体に対して2質量%含有させた。光開始剤は、1-ヒドロキシ-シクロヘキシル-フェニル-ケトン(Irgacure184)、2,4,6-トリメチルベンゾイル-ジフェニルーフォスフィンオキサイド(ルシリンTPO)を添加した。製造における酸素濃度は0.01%~22%で調整し、紫外線照射量は80mJ/cm2以下とした。
前記のようにして得られた光ファイバ着色心線を12本並列に並べて、図3ないし図5に示すような構造となるように、特許第6169060号に示される製造装置及び製造方法により、塗布ロールとして図7及び図8、塗布ロール近傍の装置として図10に示したものを用い、間欠連結部を構成する材料(紫外線硬化樹脂組成物)を下記の材料として、下記のように200m/分、400m/分、600m/分の3種類の線速(光ファイバ着色心線を進行させる速度のこと。以下同じ。)を用いて、所定のパターン(間欠連結部の長さ:30mm、非連結部の長さ:10mm、ピッチの長さ:80mm)となるように樹脂圧(塗布圧)を調整しながら塗布し、硬化させることにより間欠連結部(及び非連結部)を形成し、光ファイバテープ心線とした。
紫外線硬化樹脂としてのオリゴマー(重量平均分子量2000のポリプロピレングリコールを中間ブロックとし、骨格成分として、その両末端の水酸基に、トリレンジイソシアネートを介して、ヒドロキシエチルアクリレートを結合させたオリゴマーのこと。)、単官能モノマーとしてイソボルニルアクリレート、PO変性ノニルフェノールアクリレート、二官能モノマーとしてトリシクロデカンジメチロールジアクリレート、1,6-ヘキサンジオールジアクリレートを使用した。光開始剤として、1-ヒドロキシ-シクロヘキシル-フェニル-ケトン、2,4,6-トリメチルベンゾイル-ジフェニル-フォスフィンオキサイドを使用した。また、光安定剤としてヒンダードアミン光安定剤、シリコーン(重量平均分子量:約10000)を添加剤として適当量混合した。これらの成分で構成される材料をベース材料とし、下記に示すポリオールやレオロジーコントロール剤をそれぞれ所定の含有量で添加するようにして間欠連結部を構成する材料(紫外線硬化樹脂組成物)とした(比較例1ではポリオール、比較例2ではレオロジーコントロール剤のみ添加。)。
前記ベース材料に、ポリオールとして重量平均分子量が3000のポリプロピレングリコール(PP3000:三洋化成工業(株)製)を、紫外線硬化樹脂組成物(間欠連結部を構成する材料であり、以下、単に「組成物」とする場合もある。)全体に対して23質量%添加した。また、レオロジーコントロール剤として疎水性ヒュームドシリカ(AEROSIL R974:日本アエロジル(株)製)を組成物全体に対して5質量%添加した。
前記ベース材料に、ポリオールとして重量平均分子量が3000のポリプロピレングリコール(PP3000:三洋化成工業(株)製)を、組成物全体に対して23質量%添加した。また、レオロジーコントロール剤として疎水性ヒュームドシリカ(AEROSIL R974:日本アエロジル(株)製)を組成物全体に対して4質量%添加した。
前記ベース材料に、ポリオールとして重量平均分子量が3000のポリプロピレングリコール(PP3000:三洋化成工業(株)製)を、組成物全体に対して25質量%添加した。また、レオロジーコントロール剤として疎水性ヒュームドシリカ(AEROSIL R974:日本アエロジル(株)を組成物全体に対して6質量%添加した。
前記ベース材料に、ポリオールとして重量平均分子量が3000のポリプロピレングリコール(PP3000:三洋化成工業(株)製)を、組成物全体に対して20質量%添加した。また、レオロジーコントロール剤として疎水性ヒュームドシリカ(AEROSIL R974:日本アエロジル(株)製)を組成物全体に対して5質量%添加した。
前記ベース材料に、ポリオールとして重量平均分子量が3000のポリプロピレングリコール(PP3000:三洋化成工業(株)製)を、組成物全体に対して4質量%添加した。また、レオロジーコントロール剤として、疎水性ヒュームドシリカ(AEROSIL R974:日本アエロジル(株)製)を組成物全体に対して1質量%添加した。
前記ベース材料に、ポリオールとして重量平均分子量が3000のポリプロピレングリコール(PP3000:三洋化成工業(株)製)を、組成物全体に対して30質量%添加した。また、レオロジーコントロール剤として疎水性ヒュームドシリカ(AEROSIL R974:日本アエロジル(株)製)を組成物全体に対して10質量%添加した。
前記ベース材料に、ポリオールとして重量平均分子量が3000のポリプロピレングリコール(PP3000:三洋化成工業(株)製)を、組成物全体に対して23質量%添加した。また、レオロジーコントロール剤として親水性ヒュームドシリカ(AEROSIL 200:日本アエロジル(株)製)を組成物全体に対して5質量%添加した。
前記ベース材料に、ポリオールとして重量平均分子量が3000のポリプロピレングリコール(PP3000:三洋化成工業(株)製)を、組成物全体に対して23質量%添加した。なお、レオロジーコントロール剤は添加しなかった。
前記ベース材料に、レオロジーコントロール剤として疎水性ヒュームドシリカ(AEROSIL R974:日本アエロジル(株)製)を組成物全体に対して5質量%添加した。なお、ポリオールは添加しなかった。
前記ベース材料に、ポリオールとして重量平均分子量が3000のポリプロピレングリコール(PP3000:三洋化成工業(株)製)を、組成物全体に対して17質量%添加した。また、レオロジーコントロール剤として疎水性ヒュームドシリカ(AEROSIL R974:日本アエロジル(株)製)を組成物全体に対して0.5質量%添加した。
レオメータ(MCR301: Anton Paar社)を使用して、低せん断速度域から高せん断速度領域の粘度を測定した。25φパラレルプレート、ギャップ 0.5mm、周波数 62.8~0.68rad/s(10~0.1Hz 対数4点/桁 全9点)、歪量 5%、温度 -50℃~50℃(10℃刻み。)の条件で、周波数分散(周波数と粘度の関係)を求めた。
前記した装置を使用して間欠連結部の形成の際に間欠連結部を構成する材料を2本の光ファイバ着色心線の間に塗布する際の材料のロールからの飛散の有無を、線速を200、400、600m/分の3種類として、長さ50kmの飛散をアクリルケースで覆い確認した。ロール部分及びその他パスラインを汚染しないで50km塗布でき、安定した塗布量であったと判断できる場合を「○」、飛散が多く確認され、光ファイバ着色心線に垂れる状態やロール部分及びその他パスラインを汚染し、50km塗布しきれなかった場合を「×」として判定した。3種類の線速の全てで「○」と判定された場合、総合も「○」とした。一方、3種類の線速の少なくとも1つで「×」と判定された場合、総合も「×」とした。
間欠連結部が形成された2本の光ファイバ着色心線を取り出し、かかる光ファイバ着色心線を引張試験機の上部に固定し、2本の光ファイバ着色心線の間にφ0.5mmの針金を通し、針金を下方向に100mm/分の速度で引っ張って間欠連結部から光ファイバ着色心線を剥離させるために必要な強度(N)を計測して、光ファイバ着色心線と間欠連結部との間の接着強度とした。なお、測定対象は、600m/分で製造した光ファイバテープ心線とした。
塗布ロールの接地側と裏面、及び断面状態については、デジタルマイクロスコープ VHX-5000((株)キーエンス製)を使用して観察した。材料(樹脂組成物)が隣り合う光ファイバ着色心線の表面と裏面に良好に塗布されている場合を「○」、実用上問題ないが一方の面への塗布が不足する場合を「△」、一方の面への塗布が過度に不足し、実用上問題があると判断された場合を「×」として判定した。
樹脂組成物の対するレオロジーコントロール剤の混合及び脱泡は、攪拌・脱泡装置(ARE310:(株)シンキー製)を用いて、回転数を2000rpmとして行った。その後、スピンコーター1H-DX-2(ミカサ(株)製)を使用してガラス基板に35μmになるように回転数を設定してスピンコートを行った。その際の混合の度合い及び塗布性について、樹脂組成物に対してレオロジーコントロール剤が良好に混合、分散されているかを目視で確認し、平滑に分散され良好であると判断された場合を「○」、実用上問題ないが、流れ等が表面に確認され分散がやや悪い状態と判断される場合を「△」、分散が悪い状態と判断される場合を「×」として判定した。

実施例1の光ファイバテープ心線を用いて、光ファイバケーブルを下記のようにして製造した。
12心の光ファイバテープ心線を8本撚り合わせた光ファイバユニットを18本(または36本)撚り合わせてケーブルコアとし、その周囲に緩衝層として不織布押さえ巻テープを巻き付けた。さらに、緩衝層の外周に、φ4mmのFRP及び鋼線2本と、引き裂き紐2本とともに、被覆層を形成した。ケーブル化については、被覆層(シース)として熱可塑性樹脂を被覆し、図11の構造(光ファイバユニットの数は異なる。)のケーブルとした。
1a~1l …… 光ファイバ着色心線
10 …… 光ファイバ(ガラス光ファイバ)
11 …… 一次被覆層(プライマリ層)
12 …… 二次被覆層(セカンダリ層)
12a …… 着色された二次被覆層
13 …… 着色層
2 …… 光ファイバテープ心線
21 …… 光ファイバユニット
3 …… 間欠連結部
31,32 …… 間欠連結部
33,X …… 非連結部(単心部)
4 …… 光ファイバケーブル
41 …… ケーブルコア
42 …… 緩衝層
43 …… 鋼線(テンションメンバ)
44 …… 引き裂き紐
46 …… 被覆層(シース)
5 …… ルースチューブ
6 …… 塗布ロール
61 …… 塗布孔
62 …… 小孔
7 …… V溝ロール
71 …… V溝
8 …… エアシリンダ
9 …… ダイス
D …… 装置
R …… 間欠連結部を構成する材料
t1~t11 …… 光ファイバ着色心線対
Claims (7)
- 光ファイバの周囲に当該光ファイバを被覆する少なくとも2つの被覆層が形成され、当該被覆層のうち最外層が着色されて構成される光ファイバ着色心線を並列に配置し、隣接する前記光ファイバ着色心線が、間欠連結部によって長さ方向に連結されてなる光ファイバテープ心線であって、
前記間欠連結部が、重量平均分子量が2500~4000のポリオールを含有し、かつ、
低せん断速度域と高せん断速度域の間のニュートン域を高せん断領域側にシフトさせるレオロジーコントロール剤を前記間欠連結部全体に対して1~10質量%含有したことを特徴とする光ファイバテープ心線。 - 前記間欠連結部が、前記ポリオールを前記間欠連結部全体に対して4~30質量%含有することを特徴とする請求項1に記載の光ファイバテープ心線。
- 前記レオロジーコントロール剤が疎水性のヒュームドシリカであることを特徴とする請求項1または請求項2に記載の光ファイバテープ心線。
- 前記間欠連結部を形成する材料の粘度が、25℃での動的粘弾性から求めたせん断速度101 1/sの粘度が3~11Pa・sであり、かつ、25℃での動的粘弾性から求めたせん断速度106 1/sの粘度が0.2~2.5Pa・sであることを特徴とする請求項1ないし請求項3のいずれかに記載の光ファイバテープ心線。
- 前記25℃での動的粘弾性から求めたせん断速度101 1/sの粘度と、35℃での動的粘弾性から求めたせん断速度101 1/sの粘度の比(25℃の粘度/35℃の粘度)が3以下であることを特徴とする請求項4に記載の光ファイバテープ心線。
- 前記光ファイバ着色心線と前記間欠連結部との間の接着強度が0.07N以上であることを特徴とする請求項1ないし請求項5のいずれかに記載の光ファイバテープ心線。
- 請求項1ないし請求項6のいずれかに記載の光ファイバテープ心線を備えたことを特徴とする光ファイバケーブル。
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP19763798.6A EP3764140A4 (en) | 2018-03-08 | 2019-03-08 | FIBER TAPE AND FIBER CABLE |
| CN201980017969.0A CN111837064A (zh) | 2018-03-08 | 2019-03-08 | 光纤带芯线和光纤线缆 |
| JP2020504068A JP7288429B2 (ja) | 2018-03-08 | 2019-03-08 | 光ファイバテープ心線及び光ファイバケーブル |
| US17/014,722 US11105992B2 (en) | 2018-03-08 | 2020-09-08 | Optical fiber ribbon and optical fiber cable |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2018-041422 | 2018-03-08 | ||
| JP2018041422 | 2018-03-08 |
Related Child Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| US17/014,722 Continuation US11105992B2 (en) | 2018-03-08 | 2020-09-08 | Optical fiber ribbon and optical fiber cable |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2019172443A1 true WO2019172443A1 (ja) | 2019-09-12 |
Family
ID=67847210
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2019/009481 Ceased WO2019172443A1 (ja) | 2018-03-08 | 2019-03-08 | 光ファイバテープ心線及び光ファイバケーブル |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US11105992B2 (ja) |
| EP (1) | EP3764140A4 (ja) |
| JP (1) | JP7288429B2 (ja) |
| CN (1) | CN111837064A (ja) |
| WO (1) | WO2019172443A1 (ja) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2021019908A1 (ja) * | 2019-07-26 | 2021-02-04 | 住友電気工業株式会社 | 光ファイバリボン及び光ファイバケーブル |
| JPWO2022054940A1 (ja) * | 2020-09-14 | 2022-03-17 | ||
| JP7052100B1 (ja) | 2021-01-25 | 2022-04-11 | 古河電気工業株式会社 | 光ファイバテープ心線 |
| US11914186B2 (en) | 2018-04-16 | 2024-02-27 | Sumitomo Electric Industries, Ltd. | Optical fiber |
| WO2025163794A1 (ja) * | 2024-01-31 | 2025-08-07 | 住友電気工業株式会社 | 光ファイバケーブル |
Families Citing this family (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11415753B2 (en) * | 2020-04-30 | 2022-08-16 | Corning Research & Development Corporation | High-density FAUs and optical interconnection devices and related methods |
| EP4248250A4 (en) * | 2020-11-19 | 2024-10-30 | Corning Research & Development Corporation | INTERMITTENTLY BOUND TAPE WITH CONTINUOUS LENGTHWISE COATING |
| US11953743B2 (en) * | 2021-11-29 | 2024-04-09 | Sterlite Technologies Limited | Optical fibre ribbon with optimized number of bonds |
| CN114217398B (zh) * | 2021-12-20 | 2023-03-24 | 长飞光纤光缆股份有限公司 | 柔性光纤带的成型方法及用于实施该成型方法的点胶设备 |
| CN115308862B (zh) * | 2022-08-08 | 2023-08-25 | 富通特种光缆(天津)有限公司 | 一种可卷绕光纤带及其点胶装置 |
| AU2023203763A1 (en) * | 2022-11-24 | 2024-06-13 | Sterlite Technologies Limited | Optical fiber ribbon with a passive layer |
Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5117519B1 (ja) | 1975-02-28 | 1976-06-02 | ||
| JPS5149230B2 (ja) | 1971-09-27 | 1976-12-25 | ||
| JPS62501587A (ja) * | 1985-01-31 | 1987-06-25 | アメリカン テレフオン アンド テレグラフ カムパニ− | グリ−ス組成物を含むケ−ブル |
| US4839970A (en) * | 1985-07-05 | 1989-06-20 | Siemens Aktiengesellschaft | Filling compound for light waveguide leads and/or light waveguide cables |
| JPH02118608A (ja) * | 1988-10-28 | 1990-05-02 | Sumitomo Electric Ind Ltd | 光フアイバテープ心線 |
| JPH03256013A (ja) * | 1990-03-06 | 1991-11-14 | Sumitomo Electric Ind Ltd | ルースチューブ型光ファイバユニット |
| JP2001264604A (ja) | 2000-03-21 | 2001-09-26 | Fujikura Ltd | 光ファイバテープ心線の製造装置 |
| JP2016133606A (ja) * | 2015-01-19 | 2016-07-25 | 古河電気工業株式会社 | 光ファイバテープ心線、光ファイバテープ心線の分割方法 |
| WO2017094560A1 (ja) * | 2015-12-01 | 2017-06-08 | 古河電気工業株式会社 | 光ファイバテープ心線及び光ファイバケーブル |
| JP6169060B2 (ja) | 2014-10-16 | 2017-07-26 | 古河電気工業株式会社 | 光ファイバテープ心線の製造方法、光ファイバテープ心線の製造装置 |
| JP2017156558A (ja) * | 2016-03-02 | 2017-09-07 | 古河電気工業株式会社 | 光ファイバケーブルの製造方法、光ファイバテープ心線の製造方法 |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5373578A (en) * | 1993-12-21 | 1994-12-13 | At&T Corp. | Strippable coating for optical fiber |
| US5949940A (en) * | 1997-05-27 | 1999-09-07 | Corning Incorporated | Enhanced ribbon strippability using coating additives |
| US7257299B2 (en) * | 2005-11-30 | 2007-08-14 | Corning Incorporated | Optical fiber ribbon with improved stripability |
| JP2007272060A (ja) * | 2006-03-31 | 2007-10-18 | Furukawa Electric Co Ltd:The | 光ファイバリボン芯線及び光ファイバケーブル |
| JP5149230B2 (ja) | 2008-06-23 | 2013-02-20 | 株式会社フジクラ | 光ファイバテープ心線の製造方法及びその製造装置 |
| EP2454623A1 (en) * | 2009-07-17 | 2012-05-23 | Corning Cable Systems LLC | Optical fiber ribbons and ribbon matrix materials having low oligomer content |
| JP5117519B2 (ja) | 2010-02-16 | 2013-01-16 | 古河電気工業株式会社 | 光ファイバテープ心線及び光ファイバケーブル |
| CN107076945A (zh) * | 2014-10-17 | 2017-08-18 | 住友电气工业株式会社 | 光纤芯线及光纤带芯线 |
| JP2018504629A (ja) * | 2014-12-19 | 2018-02-15 | ダウ グローバル テクノロジーズ エルエルシー | 設計された微小構造を有するケーブルジャケット及び設計された微小構造を有するケーブルジャケットを製作するための方法 |
-
2019
- 2019-03-08 JP JP2020504068A patent/JP7288429B2/ja active Active
- 2019-03-08 EP EP19763798.6A patent/EP3764140A4/en not_active Withdrawn
- 2019-03-08 WO PCT/JP2019/009481 patent/WO2019172443A1/ja not_active Ceased
- 2019-03-08 CN CN201980017969.0A patent/CN111837064A/zh active Pending
-
2020
- 2020-09-08 US US17/014,722 patent/US11105992B2/en active Active
Patent Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS5149230B2 (ja) | 1971-09-27 | 1976-12-25 | ||
| JPS5117519B1 (ja) | 1975-02-28 | 1976-06-02 | ||
| JPS62501587A (ja) * | 1985-01-31 | 1987-06-25 | アメリカン テレフオン アンド テレグラフ カムパニ− | グリ−ス組成物を含むケ−ブル |
| US4839970A (en) * | 1985-07-05 | 1989-06-20 | Siemens Aktiengesellschaft | Filling compound for light waveguide leads and/or light waveguide cables |
| JPH02118608A (ja) * | 1988-10-28 | 1990-05-02 | Sumitomo Electric Ind Ltd | 光フアイバテープ心線 |
| JPH03256013A (ja) * | 1990-03-06 | 1991-11-14 | Sumitomo Electric Ind Ltd | ルースチューブ型光ファイバユニット |
| JP2001264604A (ja) | 2000-03-21 | 2001-09-26 | Fujikura Ltd | 光ファイバテープ心線の製造装置 |
| JP6169060B2 (ja) | 2014-10-16 | 2017-07-26 | 古河電気工業株式会社 | 光ファイバテープ心線の製造方法、光ファイバテープ心線の製造装置 |
| JP2016133606A (ja) * | 2015-01-19 | 2016-07-25 | 古河電気工業株式会社 | 光ファイバテープ心線、光ファイバテープ心線の分割方法 |
| WO2017094560A1 (ja) * | 2015-12-01 | 2017-06-08 | 古河電気工業株式会社 | 光ファイバテープ心線及び光ファイバケーブル |
| JP2017156558A (ja) * | 2016-03-02 | 2017-09-07 | 古河電気工業株式会社 | 光ファイバケーブルの製造方法、光ファイバテープ心線の製造方法 |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP3764140A4 |
Cited By (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11914186B2 (en) | 2018-04-16 | 2024-02-27 | Sumitomo Electric Industries, Ltd. | Optical fiber |
| WO2021019908A1 (ja) * | 2019-07-26 | 2021-02-04 | 住友電気工業株式会社 | 光ファイバリボン及び光ファイバケーブル |
| JPWO2021019908A1 (ja) * | 2019-07-26 | 2021-02-04 | ||
| JP7509147B2 (ja) | 2019-07-26 | 2024-07-02 | 住友電気工業株式会社 | 光ファイバリボン及び光ファイバケーブル |
| JPWO2022054940A1 (ja) * | 2020-09-14 | 2022-03-17 | ||
| WO2022054940A1 (ja) * | 2020-09-14 | 2022-03-17 | 住友電気工業株式会社 | 光ファイバテープ心線および光ファイバテープ心線の製造方法 |
| JP7052100B1 (ja) | 2021-01-25 | 2022-04-11 | 古河電気工業株式会社 | 光ファイバテープ心線 |
| JP2022113420A (ja) * | 2021-01-25 | 2022-08-04 | 古河電気工業株式会社 | 光ファイバテープ心線 |
| WO2025163794A1 (ja) * | 2024-01-31 | 2025-08-07 | 住友電気工業株式会社 | 光ファイバケーブル |
Also Published As
| Publication number | Publication date |
|---|---|
| JP7288429B2 (ja) | 2023-06-07 |
| CN111837064A (zh) | 2020-10-27 |
| US20200400903A1 (en) | 2020-12-24 |
| EP3764140A4 (en) | 2021-07-21 |
| EP3764140A1 (en) | 2021-01-13 |
| US11105992B2 (en) | 2021-08-31 |
| JPWO2019172443A1 (ja) | 2021-02-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US11105992B2 (en) | Optical fiber ribbon and optical fiber cable | |
| JP6490805B2 (ja) | 光ファイバテープ心線及び光ファイバケーブル | |
| WO2019172444A1 (ja) | 光ファイバテープ心線及び光ファイバケーブル | |
| US8406596B2 (en) | Optical fiber containing multi-layered coating system | |
| EP3221062B1 (en) | Low density uv-curable optical fiber coating, fiber made therewith, and method of fiber manufacture | |
| JP2005503593A (ja) | 感圧接着剤の特性を持つ光ファイバコーティング | |
| US20110300367A1 (en) | Optical Fiber With Photoacid Coating | |
| EP4289876A1 (en) | Resin composition, optical fiber, optical fiber manufacturing method, optical fiber ribbon, and optical fiber cable | |
| JP6046021B2 (ja) | オーバーコート心線及び当該オーバーコート心線を備えた光ファイバケーブル | |
| CN116568651B (zh) | 树脂组合物、树脂组合物的制造方法、光纤、光纤的制造方法、光纤带以及光纤缆线 | |
| JP7335903B2 (ja) | 光ファイバテープ心線及び光ファイバケーブル | |
| JP5787927B2 (ja) | オーバーコート心線及び当該オーバーコート心線を備えた光ファイバケーブル | |
| WO2002075419A1 (fr) | Coeur rubane de fibre optique de type fendu | |
| CN115836239A (zh) | 树脂组合物、光纤以及光纤的制造方法 | |
| JP5871435B2 (ja) | オーバーコート心線及び当該オーバーコート心線を備えた光ファイバケーブル | |
| JP2002341209A (ja) | 分割型光ファイバテープ心線の製造方法 | |
| JP3493836B2 (ja) | 紫外線硬化型光ファイバ用テープ化材組成物及び光ファイバ用テープ化材 | |
| CN120936583A (zh) | 树脂组合物、光纤、光纤的制造方法、光纤带、及光纤线缆 | |
| JP2020052286A (ja) | 光ファイバオーバーコート心線及び光ファイバコード |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 19763798 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2020504068 Country of ref document: JP Kind code of ref document: A |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2019763798 Country of ref document: EP |
|
| ENP | Entry into the national phase |
Ref document number: 2019763798 Country of ref document: EP Effective date: 20201008 |