WO2022054660A1 - ガラス繊維強化樹脂板 - Google Patents
ガラス繊維強化樹脂板 Download PDFInfo
- Publication number
- WO2022054660A1 WO2022054660A1 PCT/JP2021/032095 JP2021032095W WO2022054660A1 WO 2022054660 A1 WO2022054660 A1 WO 2022054660A1 JP 2021032095 W JP2021032095 W JP 2021032095W WO 2022054660 A1 WO2022054660 A1 WO 2022054660A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- glass fiber
- reinforced resin
- resin plate
- fiber reinforced
- glass
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Classifications
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08J—WORKING-UP; GENERAL PROCESSES OF COMPOUNDING; AFTER-TREATMENT NOT COVERED BY SUBCLASSES C08B, C08C, C08F, C08G or C08H
- C08J5/00—Manufacture of articles or shaped materials containing macromolecular substances
- C08J5/18—Manufacture of films or sheets
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08J—WORKING-UP; GENERAL PROCESSES OF COMPOUNDING; AFTER-TREATMENT NOT COVERED BY SUBCLASSES C08B, C08C, C08F, C08G or C08H
- C08J5/00—Manufacture of articles or shaped materials containing macromolecular substances
- C08J5/04—Reinforcing macromolecular compounds with loose or coherent fibrous material
- C08J5/0405—Reinforcing macromolecular compounds with loose or coherent fibrous material with inorganic fibres
- C08J5/043—Reinforcing macromolecular compounds with loose or coherent fibrous material with inorganic fibres with glass fibres
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08K—Use of inorganic or non-macromolecular organic substances as compounding ingredients
- C08K7/00—Use of ingredients characterised by shape
- C08K7/02—Fibres or whiskers
- C08K7/04—Fibres or whiskers inorganic
- C08K7/14—Glass
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08K—Use of inorganic or non-macromolecular organic substances as compounding ingredients
- C08K9/00—Use of pretreated ingredients
- C08K9/04—Ingredients treated with organic substances
- C08K9/06—Ingredients treated with organic substances with silicon-containing compounds
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08L—COMPOSITIONS OF MACROMOLECULAR COMPOUNDS
- C08L77/00—Compositions of polyamides obtained by reactions forming a carboxylic amide link in the main chain; Compositions of derivatives of such polymers
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08J—WORKING-UP; GENERAL PROCESSES OF COMPOUNDING; AFTER-TREATMENT NOT COVERED BY SUBCLASSES C08B, C08C, C08F, C08G or C08H
- C08J2333/00—Characterised by the use of homopolymers or copolymers of compounds having one or more unsaturated aliphatic radicals, each having only one carbon-to-carbon double bond, and only one being terminated by only one carboxyl radical, or of salts, anhydrides, esters, amides, imides, or nitriles thereof; Derivatives of such polymers
- C08J2333/24—Homopolymers or copolymers of amides or imides
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08J—WORKING-UP; GENERAL PROCESSES OF COMPOUNDING; AFTER-TREATMENT NOT COVERED BY SUBCLASSES C08B, C08C, C08F, C08G or C08H
- C08J2367/00—Characterised by the use of polyesters obtained by reactions forming a carboxylic ester link in the main chain; Derivatives of such polymers
- C08J2367/02—Polyesters derived from dicarboxylic acids and dihydroxy compounds
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08J—WORKING-UP; GENERAL PROCESSES OF COMPOUNDING; AFTER-TREATMENT NOT COVERED BY SUBCLASSES C08B, C08C, C08F, C08G or C08H
- C08J2377/00—Characterised by the use of polyamides obtained by reactions forming a carboxylic amide link in the main chain; Derivatives of such polymers
- C08J2377/02—Polyamides derived from omega-amino carboxylic acids or from lactams thereof
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08J—WORKING-UP; GENERAL PROCESSES OF COMPOUNDING; AFTER-TREATMENT NOT COVERED BY SUBCLASSES C08B, C08C, C08F, C08G or C08H
- C08J2381/00—Characterised by the use of macromolecular compounds obtained by reactions forming in the main chain of the macromolecule a linkage containing sulfur with or without nitrogen, oxygen, or carbon only; Polysulfones; Derivatives of such polymers
- C08J2381/04—Polysulfides
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08K—Use of inorganic or non-macromolecular organic substances as compounding ingredients
- C08K2201/00—Specific properties of additives
- C08K2201/002—Physical properties
- C08K2201/003—Additives being defined by their diameter
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08K—Use of inorganic or non-macromolecular organic substances as compounding ingredients
- C08K2201/00—Specific properties of additives
- C08K2201/002—Physical properties
- C08K2201/004—Additives being defined by their length
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08K—Use of inorganic or non-macromolecular organic substances as compounding ingredients
- C08K2201/00—Specific properties of additives
- C08K2201/016—Additives defined by their aspect ratio
Definitions
- the present invention relates to a glass fiber reinforced resin plate.
- a glass fiber reinforced resin molded product containing glass fiber having a flat cross-sectional shape is more portable than a glass fiber reinforced resin molded product containing glass fiber having a circular cross section because it suppresses warpage and is superior in dimensional stability. It is widely used for light, thin, short and small materials such as electronic device housings (see, for example, Patent Document 1).
- Patent Document 2 On the other hand, in recent years, attention has been focused on composite materials of metals and plate-shaped fiber reinforced resin molded products, mainly for automobile applications (see, for example, Patent Document 2).
- a glass fiber reinforced resin plate containing glass fiber having a flat cross-sectional shape has excellent dimensional stability and has higher mechanical strength than a glass fiber reinforced resin plate containing glass fiber having a circular cross section. , It is considered that it can also be used for composite material applications with metals.
- a glass fiber reinforced resin plate containing glass fiber having a flat cross-sectional shape in a composite material of a metal and a fiber reinforced resin molded product which is thicker than a light, thin, short and small material such as a portable electronic device housing which has been conventionally used.
- a glass fiber reinforced resin plate containing glass fiber having a flat cross-sectional shape in a composite material of a metal and a fiber reinforced resin molded product, which is thicker than a light, thin, short and small material such as a portable electronic device housing which has been conventionally used.
- the TD direction refers to a direction orthogonal to the direction in which the resin composition flows when the resin composition containing glass fibers is molded to produce a glass fiber reinforced resin plate.
- the MD direction refers to the direction in which the resin composition flows when the resin composition containing the glass fiber is molded to produce the glass fiber reinforced resin plate.
- the present invention is to solve this inconvenience and provide a glass fiber reinforced resin plate containing a glass fiber having a flat cross-sectional shape and having an improved elastic modulus in the TD direction.
- the present invention is a glass fiber reinforced resin plate containing a glass fiber having a flat cross-sectional shape and a resin, and the glass fiber having the flat cross-sectional shape has a minor axis of 4. It is in the range of 5 to 10.5 ⁇ m, the major axis is in the range of 22.0 to 80.0 ⁇ m, and the ratio of the major axis to the minor axis (major axis / minor axis) R is in the range of 4.5 to 10.0.
- the glass fiber content C in the glass fiber reinforced resin plate is in the range of 5.0 to 75.0% by mass, and the thickness H of the glass fiber reinforced resin plate is in the range of more than 0.5 mm and 10.0 mm or less.
- the present invention is characterized in that C and H satisfy the following formula (1).
- the glass fiber reinforced resin plate of the present invention contains a glass fiber having a flat cross-sectional shape and a resin.
- the glass fiber having the flat cross-sectional shape has a minor axis in the range of 4.5 to 10.5 ⁇ m and a major axis in the range of 22.0 to 80.0 ⁇ m, and the ratio of the major axis to the minor axis.
- the (major axis / minor axis) R is in the range of 4.5 to 10.0.
- the elastic modulus in the TD direction becomes insufficient, so that an imbalance occurs between the elastic modulus in the TD direction and the elastic modulus in the MD direction. Due to the imbalance, there is a concern that the adhesiveness with the metal will decrease.
- the glass fiber reinforced resin plate of the present invention has a glass fiber content C in the range of 5.0 to 75.0 mass% and a thickness H in the range of more than 0.5 mm and 10.0 mm or less.
- the elastic modulus in the TD direction can be improved.
- the elastic modulus in the TD direction can be improved by comparing the elastic modulus in the TD direction of the glass fiber reinforced resin plate of the present invention with the elastic modulus in the TD direction of the glass fiber reinforced resin plate to be compared. This means that the elastic modulus in the TD direction is improved by 5.0% or more.
- the glass fiber reinforced resin plate to be compared has the same cross-sectional area as the glass fiber used in the glass fiber reinforced resin plate of the present invention, and the ratio of the major axis to the minor axis (major axis / minor axis) R is 4.0.
- the glass fiber reinforced resin plate of the present invention has an elastic modulus in the TD direction when the product of C and H is less than 30.0 or more than 120.0 when the glass fiber content C and the thickness H are in the above ranges. Cannot be improved.
- the glass fiber content C is in the range of 20.0 to 60.0% by mass, and the thickness H of the glass fiber reinforced resin plate is 0.8 to 8. It is preferable that the C and H are in the range of 0 mm and satisfy the following formula (2).
- the elastic modulus in the TD direction can be further improved by satisfying the following formula (2) when the C and H are in the above range.
- the elastic modulus in the TD direction can be further improved by the elastic modulus in the TD direction of the glass fiber reinforced resin plate of the present invention and the elastic modulus in the TD direction of the glass fiber reinforced resin plate to be compared. It means that the elastic modulus in the TD direction is improved by 10.0% or more.
- the glass fiber content C is in the range of 20.0 to 40.0% by mass, and the glass fiber reinforced. It is more preferable that the thickness H of the resin plate is in the range of 1.6 to 5.0 mm, and the C and H satisfy the following formula (3).
- the resin contained in the glass fiber reinforced resin plate is preferably a crystalline thermoplastic resin, and is preferably polyamide. Is even more preferable.
- the glass fiber reinforced resin plate of the present embodiment is a molded product containing a glass fiber having a flat cross-sectional shape and a resin.
- the glass composition of the glass forming the glass fiber is not particularly limited.
- the glass composition that can be taken by the glass fiber is the most general-purpose E glass composition, high strength and high elasticity glass composition, high elasticity and easy-to-manufacture glass composition, and low dielectric.
- the composition of low-conductivity positive contact glass can be mentioned.
- the E glass composition has a total of 20. SiO 2 in the range of 52.0 to 56.0% by mass and Al 2 O 3 in the range of 12.0 to 16.0% by mass with respect to the total amount of glass fiber. It is a composition containing MgO and CaO in the range of 0 to 25.0% by mass, and B 2O 3 in the range of 5.0 to 10.0% by mass.
- the high-strength and high-elasticity glass composition has SiO 2 in the range of 60.0 to 70.0% by mass and Al 2 O 3 in the range of 20.0 to 30.0% by mass with respect to the total amount of glass fibers.
- MgO in the range of 5.0 to 15.0% by mass
- Fe 2 O 3 in the range of 0 to 1.5% by mass
- Na 2 O, K 2 O and K 2 O in the range of 0 to 0.2% by mass in total. It is a composition containing Li 2 O.
- the highly elastic and easy-to-manufacture glass composition has SiO 2 in the range of 57.0 to 60.0% by mass and Al 2O in the range of 17.5 to 20.0% by mass with respect to the total amount of glass fibers. 3 , MgO in the range of 8.5 to 12.0% by mass, CaO in the range of 10.0 to 13.0% by mass, and B 2 O 3 in the range of 0.5 to 1.5% by mass.
- the composition is such that the total amount of SiO 2 , Al 2 O 3 , MgO and CaO is 98.0% by mass or more.
- the low dielectric constant and low dielectric normal contact glass composition has SiO 2 in the range of 48.0 to 62.0% by mass and B 2 O 3 in the range of 17.0 to 26.0% by mass with respect to the total amount of glass fibers.
- Al 2 O 3 in the range of 9.0 to 18.0 mass%
- CaO in the range of 0.1 to 9.0 mass%
- MgO in the range of 0 to 6.0 mass%, in total.
- Na 2 O, K 2 O and Li 2 O in the range of 0.05 to 0.5% by mass
- TiO 2 in the range of 0 to 5.0% by mass
- SrO in the range of 0 to 6.0% by mass.
- F 2 and Cl 2 in the range of 0 to 3.0% by mass in total
- P 2 O 5 in the range of 0 to 6.0% by mass.
- the glass composition of the glass fiber is preferably the high-strength high elastic modulus glass composition or the high elastic modulus easy-to-manufacture glass composition. Further, the glass composition of the glass fiber reduces the dielectric constant and the dielectric loss tangent of the glass fiber reinforced resin plate, and reduces the transmission loss of the high frequency signal passing through the glass fiber reinforced resin plate. It is preferably a dielectric loss tangent glass composition.
- each component of the glass composition described above can be measured by using an ICP emission spectroscopic analyzer for Li, which is a light element, and by using a wavelength dispersive fluorescent X-ray analyzer for other elements. ..
- a measurement method there are the following methods.
- the glass fiber is cut into an appropriate size, placed in a platinum rut pot, kept at a temperature of 1550 ° C. for 6 hours in an electric furnace, and melted while stirring to obtain a homogeneous molten glass.
- the obtained molten glass is poured onto a carbon plate to produce a glass cullet, which is then pulverized and pulverized to obtain a glass powder.
- Li which is a light element, is quantitatively analyzed using an ICP emission spectrophotometer after heat-decomposing the glass powder with an acid. Other elements are quantitatively analyzed using a wavelength dispersive fluorescent X-ray analyzer after the glass powder is formed into a disk shape with a press machine. The content and total amount of each component can be calculated by converting these quantitative analysis results into oxides, and the content (mass%) of each component described above can be obtained from these numerical values.
- the glass fiber has an organic substance attached to the surface of the glass fiber, or when the glass fiber is mainly contained as a reinforcing material in the organic substance (resin), for example, a muffle furnace at 300 to 650 ° C. It is used after removing organic substances by heating it for about 2 to 24 hours.
- organic substance for example, a muffle furnace at 300 to 650 ° C. It is used after removing organic substances by heating it for about 2 to 24 hours.
- the glass fiber having the above-mentioned glass composition can be produced as follows. First, a glass raw material (glass batch) prepared to have the above-mentioned composition is supplied to a melting furnace and melted at a temperature in the range of, for example, 1450 to 1550 ° C. Next, the molten glass batch (molten glass) is pulled out from 1 to 30,000 nozzle tips of a bushing controlled to a predetermined temperature and rapidly cooled to form a glass filament. Next, a sizing agent or a binder is applied to the formed glass filaments using an applicator, which is a coating device, and a sizing shoe is used to squeeze 1 to 30,000 glass filaments while using a winder. Glass fiber can be obtained by winding it around a tube at high speed.
- the glass fiber having a flat cross-sectional shape used for the glass fiber reinforced resin plate of the present embodiment has the nozzle tip having a non-circular shape and having a protrusion or a notch for quenching the molten glass. It can be obtained by controlling the temperature condition. Further, the minor axis and the major axis of the glass fiber can be adjusted by adjusting the diameter of the nozzle tip, the winding speed, the temperature condition, and the like. For example, by increasing the winding speed, the minor axis and the major axis can be reduced, and by decreasing the winding speed, the minor axis and the major axis can be increased.
- the glass fiber having a flat cross-sectional shape used in the glass fiber reinforced resin plate of the present embodiment has a minor axis of 4.5 to 10.5 ⁇ m, preferably 5.0 to 8.0 ⁇ m, and more preferably 5.0 to. It is in the range of 6.4 ⁇ m and has a major axis of 22.0 to 80.0 ⁇ m, preferably 28.5 to 70.0 ⁇ m, more preferably 29.5 to 65.0 ⁇ m, still more preferably 32.5 to 60.0 ⁇ m.
- the ratio (major axis / minor axis) R of the major axis to the minor axis is 4.5 to 10.0, preferably 5.0 to 7.9, more preferably. Is in the range of 5.0 to 6.7, more preferably 5.5 to 6.5.
- the flat cross-sectional shape is preferably an elliptical shape or an oval shape, and more preferably an oval shape.
- the oval shape is a rectangle having a semicircular shape at both ends, or a shape similar thereto.
- the converted fiber diameter of the glass fiber having a flat cross-sectional shape used in the glass fiber reinforced resin plate of the present embodiment is in the range of 11.0 to 32.0 ⁇ m, preferably in the range of 12.0 to 22.0 ⁇ m. It is more preferably in the range of 12.5 to 20.0 ⁇ m, and even more preferably in the range of 13.5 to 18.0 ⁇ m.
- the converted fiber diameter means the diameter of the glass fiber having the same cross-sectional area as the cross-sectional area of the glass fiber having a flat cross-sectional shape and having a circular cross section.
- the minor axis and the major axis of the glass fiber having a flat cross-sectional shape in the glass fiber reinforced resin plate of the present embodiment can be calculated as follows, for example.
- the major axis the longest side passing through the substantially center of the glass filament cross section
- the minor axis the side orthogonal to the major axis at the substantially center of the glass filament cross section. Measure the length.
- the minor axis and the major axis of the glass fiber can be calculated by obtaining the average value of the measured values of the respective lengths of the minor axis and the major axis.
- the glass fiber is usually formed by focusing a plurality of glass filaments, but in the glass fiber reinforced resin plate, the focus is released by undergoing a molding process, and the glass is in the state of a glass filament. It is dispersed in the fiberglass reinforced resin plate.
- the number of glass filaments constituting the glass fiber is preferably 1.
- the length is preferably in the range of 20,000, more preferably 50 to 10,000, still more preferably 1,000 to 8,000, and the length of the glass fiber (also referred to as a glass fiber bundle or a glass strand) is preferably 1.0 to 100.0 mm. It was cut into a range of 1.2 to 51.0 mm, more preferably 1.5 to 30.0 mm, particularly preferably 2.0 to 15.0 mm, and most preferably 2.3 to 7.8 mm. Chopped strands can be mentioned.
- the number of glass filaments constituting the glass fiber is 10 to 10 in addition to the chopped strand.
- the length is 0.001 to 0 by a known method such as a ball mill or a hensyl mixer. Examples include cut fibers crushed to a range of .900 mm.
- Such a composition coats the glass fiber at a ratio in the range of 0.1 to 2.0% by mass based on the mass of the glass fiber in the state where it is not coated with the composition.
- the resin examples include urethane resin, epoxy resin, vinyl acetate resin, acrylic resin, modified polypropylene, particularly carboxylic acid-modified polypropylene, (poly) carboxylic acid, and a copolymer of maleic acid and an unsaturated monomer. be able to.
- the coating of the glass fiber with an organic substance includes, for example, a solution of the composition, the resin, or the silane coupling agent using a known method such as a roller type applicator in the glass fiber manufacturing process. This can be done by applying a sizing agent or a binder to the glass fiber and then drying the glass fiber to which the resin, the silane coupling agent or the composition is applied.
- examples of the silane coupling agent include aminosilane, chlorsilane, epoxysilane, mercaptosilane, vinylsilane, acrylicsilane, and cationicsilane.
- these compounds may be used alone, or two or more kinds thereof may be used in combination.
- aminosilane examples include ⁇ -aminopropyltriethoxysilane, N- ⁇ - (aminoethyl) - ⁇ -aminopropyltrimethoxysilane, and N- ⁇ - (aminoethyl) -N'- ⁇ - (aminoethyl) - ⁇ .
- -Aminopropyltrimethoxysilane, ⁇ -anilinopropyltrimethoxysilane and the like can be mentioned.
- examples of the mercaptosilane include ⁇ -mercaptotrimethoxysilane.
- acrylic silane examples include ⁇ -methacryloxypropyltrimethoxysilane.
- animal oil examples include beef tallow and the like.
- examples of the vegetable oil include soybean oil, palm oil, rapeseed oil, palm oil, castor oil and the like.
- animal wax beeswax, lanolin and the like can be mentioned.
- examples of the vegetable wax include candelilla wax and carnauba wax.
- examples of the mineral wax include paraffin wax, montan wax and the like.
- examples of the condensate of the higher saturated fatty acid and the higher saturated alcohol include stearic acid esters such as lauryl stearate.
- examples of the quaternary ammonium salt include alkyltrimethylammonium salts such as lauryltrimethylammonium chloride.
- surfactant examples include nonionic surfactants, cationic surfactants, anionic surfactants, and amphoteric surfactants.
- the surfactants may be used alone or in combination of two or more.
- Nonionic surfactants include ethylene oxide propylene oxide alkyl ethers, polyoxyethylene alkyl ethers, polyoxyethylene-polyoxypropylene-block copolymers, alkylpolyoxyethylene-polyoxypropylene-block copolymer ethers, and polyoxyethylene fatty acid esters.
- Cationic surfactants include alkyldimethylbenzylammonium chloride, alkyltrimethylammonium chloride, alkyldimethylethylammonium ethyl sulfate, higher alkylamine salts (acetates, hydrochlorides, etc.), ethylene oxide adducts to higher alkylamines, higher grades.
- alkylamine salts acetates, hydrochlorides, etc.
- ethylene oxide adducts to higher alkylamines higher grades.
- examples thereof include a condensate of a fatty acid and a polyalkylene polyamine, a salt of an ester of a higher fatty acid and an alkanolamine, a salt of a higher fatty acid amide, an imidazoline-type cationic surfactant, and an alkylpyridinium salt.
- anionic surfactants include higher alcohol sulfate ester salts, higher alkyl ether sulfate ester salts, ⁇ -olefin sulfate ester salts, alkylbenzene sulfonates, ⁇ -olefin sulfonates, and reactions of fatty acid halide with N-methyltaurine.
- anionic surfactants include higher alcohol sulfate ester salts, higher alkyl ether sulfate ester salts, ⁇ -olefin sulfate ester salts, alkylbenzene sulfonates, ⁇ -olefin sulfonates, and reactions of fatty acid halide with N-methyltaurine.
- examples thereof include products, sulfosuccinic acid dialkyl ester salts, higher alcohol phosphate ester salts, and higher alcohol ethylene oxide adduct phosphate ester salts.
- amphoteric tenside examples include an amino acid type amphoteric tenside such as an alkylaminopropionic acid alkali metal salt, a betaine type such as alkyldimethylbetaine, and an imidazoline type amphoteric tenside.
- amino acid type amphoteric tenside such as an alkylaminopropionic acid alkali metal salt
- betaine type such as alkyldimethylbetaine
- imidazoline type amphoteric tenside examples include imidazoline type amphoteric tenside.
- thermoplastic resin As the resin used for the glass fiber reinforced resin plate of the present embodiment, a thermoplastic resin can be mentioned.
- thermoplastic resin includes polyethylene, polypropylene, polystyrene, styrene / maleic anhydride resin, styrene / maleimide resin, polyacrylonitrile, acrylonitrile / styrene (AS) resin, acrylonitrile / butadiene / styrene (ABS) resin, and chlorine.
- polyethylene examples include high-density polyethylene (HDPE), medium-density polyethylene, low-density polyethylene (LDPE), linear low-density polyethylene (LLDPE), and ultra-high-molecular-weight polyethylene.
- HDPE high-density polyethylene
- LDPE low-density polyethylene
- LLDPE linear low-density polyethylene
- ultra-high-molecular-weight polyethylene examples include ultra-high-molecular-weight polyethylene.
- polypropylene examples include isotactic polypropylene, atactic polypropylene, syndiotactic polypropylene, and mixtures thereof.
- polystyrene examples include general-purpose polystyrene (GPPS) which is an atactic polystyrene having an atactic structure, impact-resistant polystyrene (HIPS) obtained by adding a rubber component to GPPS, and syndiotactic polystyrene having a syndiotactic structure. ..
- GPPS general-purpose polystyrene
- HIPS impact-resistant polystyrene
- methacrylic acid a polymer obtained by homopolymerizing one of acrylic acid, methacrylic acid, styrene, methyl acrylate, ethyl acrylate, ethyl methacrylate, butyl acrylate, butyl methacrylate, and fatty acid vinyl ester, or two or more thereof.
- examples thereof include a polymer obtained by copolymerizing the above.
- the polyvinyl chloride can be copolymerized with a vinyl chloride homopolymer polymerized by a conventionally known emulsification polymerization method, a suspension polymerization method, a microsuspension polymerization method, a bulk polymerization method, or the like, or a vinyl chloride monomer.
- a copolymer with a monomer a graft copolymer obtained by graft-polymerizing a vinyl chloride monomer to the polymer, and the like.
- polyamide examples include polycaproamide (polyamide 6), polyhexamethylene adipamide (polyamide 66), polytetramethylene adipamide (polyamide 46), polytetramethylene sebacamide (polyamide 410), and polypentamethylene adipa.
- Polyundecamethylene terephthalamide (polyamide 11T), polydodecamethylene terephthalamide (polyamide 12T), polytetramethylene isophthalamide (polyamide 4I), polybis (3-methyl-4-aminohexyl) methaneterephthalamide (polyamide PACMT) , Polybis (3-methyl-4-aminohexyl) methaneisophthalamide (polyamide PACMI), polybis (3-methyl-4-aminohexyl) methaneddecamide (polyamide PACM12), polybis (3-methyl-4-aminohexyl) Examples thereof include a copolymer in which one of the components such as methanetetradecamide (polyamide PACM14) or a plurality of two or more components are combined, a mixture thereof, and the like.
- the polyacetal includes a homopolymer having an oxymethylene unit as a main repeating unit and a copolymer containing an oxyalkylene unit having 2 to 8 adjacent carbon atoms in the main chain, which is mainly composed of an oximethylene unit. And so on.
- polyethylene terephthalate examples include a polymer obtained by polycondensing ethylene glycol with terephthalic acid or a derivative thereof.
- polybutylene terephthalate examples include a polymer obtained by polycondensing 1,4-butanediol with terephthalic acid or a derivative thereof.
- polytrimethylene terephthalate examples include a polymer obtained by polycondensing 1,3-propanediol with terephthalic acid or a derivative thereof.
- polycarbonate examples include a polymer obtained by an ester exchange method in which a dihydroxydiaryl compound and a carbonic acid ester such as diphenyl carbonate are reacted in a molten state, or a polymer obtained by a phosgene method in which a dihydroxyaryl compound and phosgene are reacted. be able to.
- polyphenylene sulfide examples include linear polyphenylene sulfide, crosslinked polyphenylene sulfide that has been polymerized by performing a curing reaction after polymerization, polyphenylene sulfide sulfone, polyphenylene sulfide ether, and polyphenylene sulfide ketone.
- polyphenylene ether examples include poly (2,3-dimethyl-6-ethyl-1,4-phenylene ether), poly (2-methyl-6-chloromethyl-1,4-phenylene ether), and poly (2-methyl-). 6-Hydroxyethyl-1,4-phenylene ether), poly (2-methyl-6-n-butyl-1,4-phenylene ether), poly (2-ethyl-6-isopropyl-1,4-phenylene ether) , Poly (2-ethyl-6-n-propyl-1,4-phenylene ether), Poly (2,3,6-trimethyl-1,4-phenylene ether), Poly [2- (4'-methylphenyl) -1,4-phenylene ether], poly (2-bromo-6-phenyl-1,4-phenylene ether), poly (2-methyl-6-phenyl-1,4-phenylene ether), poly (2-phenyl) -1,4-phenylene ether), poly (2-chlor
- the modified polyphenylene ethers include polymer alloys of poly (2,6-dimethyl-1,4-phenylene) ether and polystyrene, and poly (2,6-dimethyl-1,4-phenylene) ethers and styrene / butadiene copolymers.
- Examples thereof include those having a functional group such as a group and a styryl group introduced, and those having a functional group such as an amino group, an epoxy group, a carboxy group, a styryl group and a methacrylic group introduced into the polymer chain side chain of the polyphenylene ether. ..
- the liquid crystal polymer (LCP) has one or more structures selected from aromatic hydroxycarbonyl units, aromatic dihydroxy units, aromatic dicarbonyl units, aliphatic dihydroxy units, aliphatic dicarbonyl units and the like, which are thermotropic liquid crystal polyesters. Examples thereof include (co) polymers composed of units.
- polylactic acid examples include polyL-lactic acid, which is an L-form homopolymer, polyD-lactic acid, which is a D-form homopolymer, and stereocomplex-type polylactic acid, which is a mixture thereof.
- the resin used for the glass fiber reinforced resin plate of the present embodiment is preferably a crystalline thermoplastic resin because the effect of improving the elastic modulus in the TD direction is large.
- the crystalline thermoplastic resin include polyamide, polybutylene terephthalate, polyphenylene sulfide, polyetheretherketone, polyethylene, polypropylene and the like, but polyamide is more preferable, and polyamide 6 is particularly preferable.
- the resin used for the glass fiber reinforced resin plate of the present embodiment is the crystalline thermoplastic resin, it is preferable that the resin does not contain the amorphous thermoplastic resin.
- the glass fiber reinforced resin plate of the present embodiment When the resin used for the glass fiber reinforced resin plate of the present embodiment is a transparent resin, the glass fiber reinforced resin plate of the present embodiment has visible light, ultraviolet rays, infrared rays, and laser beams with respect to the glass fiber reinforced resin plate to be compared. It is possible to improve the light transmittance such as.
- the glass fiber reinforced resin plate to be compared has the same cross-sectional area as the glass fiber used in the glass fiber reinforced resin plate of the present embodiment, and the ratio (major axis / minor axis) R of the major axis to the minor axis is 4.0.
- the glass fiber content C and the thickness H are the same as the glass fiber reinforced resin plate of the present embodiment, and the same molding conditions as the glass fiber reinforced resin plate of the present embodiment. It is a glass fiber reinforced resin plate manufactured in.
- the transparent resin include polystyrene, ABS resin, (meth) acrylic resin, polyacetal, polyethylene terephthalate, polycarbonate, and polyarylate.
- the glass fiber reinforced resin plate of the present embodiment is, for example, a biaxial kneader in which a chopped strand having a predetermined length and a chopped strand in which glass filaments of glass fiber having a flat cross-sectional shape are focused and the resin are combined. It can be obtained by kneading at the above and performing injection molding using the obtained resin pellets. Further, the glass fiber reinforced resin plate of the present embodiment includes an injection compression molding method, a two-color molding method, a hollow molding method, a foam molding method (including a supercritical fluid foam molding method), an insert molding method, and an in-mold coating molding method.
- Extrusion molding method sheet molding method, thermal molding method, rotary molding method, laminated molding method, press molding method, blow molding method, stamping molding method, infusion method, hand lay-up method, spray-up method, resin transfer molding method, It can also be obtained by using a known molding method such as a sheet molding compound method, a bulk molding compound method, a plutrusion method, or a filament winding method.
- the shape of the glass fiber reinforced resin plate of the present embodiment obtained as described above may be a flat plate, a flat plate having holes or irregularities, or a plate having a curved surface or bending.
- a hollow cylinder, a hollow polygonal prism, and a box are included.
- the glass fiber reinforced resin plate of the present embodiment has a glass fiber content C in the range of 5.0 to 75.0 mass% and a thickness H in the range of more than 0.5 mm and 10.0 mm or less.
- C and H satisfy the following formula (1), the elastic modulus in the TD direction can be improved.
- the glass fiber content C is preferably 20.0 to 60.0% by mass, more preferably 20.0 to 40.0% by mass, and more preferably 21. It is in the range of 0.0 to 38.0% by mass.
- the thickness H of the glass fiber reinforced resin plate is preferably 0.8 to 8.0 mm, more preferably 1.6 to 5.0 mm, still more preferably 1. It is in the range of 0.6 to 3.4 mm, particularly preferably 1.6 to 2.4 mm.
- the C and H preferably satisfy the following formula (2), more preferably the following formula (3), and further preferably the following formula (4).
- the following formula (5) is satisfied, particularly preferably the following formula (6) is satisfied, and most preferably the following formula (7) is satisfied.
- the number average fiber length L of the glass fiber contained in the glass fiber reinforced resin plate of the present embodiment is in the range of 100 to 700 ⁇ m, preferably 150 to 450 ⁇ m, more preferably 200 to 400 ⁇ m, and more preferably. It is in the range of 220 to 380 ⁇ m.
- the number average fiber length L of the glass fibers contained in the glass fiber reinforced resin plate of the present embodiment is, for example, put into a twin-screw kneader when the glass fiber reinforced resin plate of the present embodiment is obtained by injection molding. It can be controlled by adjusting the length of the chopped strand to be formed and the screw rotation speed of the twin-screw kneader. For example, by lengthening the length of the chopped strand charged into the twin-screw kneader in the range of 1.0 to 100.0 mm, the L can be lengthened and the length of the chopped strand can be shortened. Therefore, the L can be shortened. Further, the L can be lengthened by lowering the screw rotation speed during biaxial kneading in the range of 10 to 1000 rpm, and the L can be shortened by increasing the rotation speed.
- glass fiber reinforced resin plate of the present embodiment examples include, but are not limited to, a plate-shaped metal substitute material for automobiles and a composite material of a metal for automobile use and a plate-shaped fiber-reinforced resin molded product. ..
- the glass fiber reinforced resin plate of the present embodiment can be preferably used, for example, for automobile exterior parts such as front fenders and door panels, automobile interior parts such as trims and glove boxes, and
- the E glass composition has an elliptical cross-sectional shape having a major axis of 34.1 ⁇ m, a minor axis of 5.7 ⁇ m, a major axis / minor axis R of 6.0, and a converted fiber diameter of 15.4 ⁇ m.
- PA is kneaded with a twin-screw kneader (manufactured by Shibaura Machinery Co., Ltd., trade name: TEM-26SS) at a screw rotation speed of 100 rpm, and resin pellets having a glass content C of 40% by mass. Was produced.
- a twin-screw kneader manufactured by Shibaura Machinery Co., Ltd., trade name: TEM-26SS
- injection molding was performed with an injection molding machine (manufactured by Nissei Resin Industry Co., Ltd., trade name: NEX80) at a mold temperature of 90 ° C. and an injection temperature of 270 ° C.
- NEX80 injection molding machine
- a glass fiber reinforced resin plate (flat plate) having a length of 80 mm and a width of 60 mm and a thickness H of 1.0 mm was produced.
- the TD direction bending elasticity and the MD direction bending elasticity are measured by the method described below, and the glass in the glass fiber reinforced resin plate is measured.
- the number average fiber length L of the fibers was calculated. The results are shown in Table 1.
- the length direction of the glass fiber reinforced resin plate corresponds to the TD direction of the glass fiber reinforced resin plate
- the width direction of the test piece corresponds to the MD direction of the glass fiber reinforced resin plate.
- a test piece was obtained by processing into a width of 25 mm and a length of 20 mm. Next, the obtained test piece was statically compliant with JIS K 7171: 2016 using a precision universal testing machine (manufactured by Shimadzu Corporation, trade name: Autograph AG-XPlus) under the condition of a test temperature of 23 ° C. A target bending test was performed, and the flexural modulus in the TD direction was measured.
- the length direction of the glass fiber reinforced resin plate corresponds to the MD direction of the glass fiber reinforced resin plate
- the width direction of the test piece corresponds to the TD direction of the glass fiber reinforced resin plate.
- a test piece was obtained by processing into a width of 25 mm and a length of 20 mm. Next, the obtained test piece was statically compliant with JIS K 7171: 2016 using a precision universal testing machine (manufactured by Shimadzu Corporation, trade name: Autograph AG-XPlus) under the condition of a test temperature of 23 ° C. A target bending test was performed, and the flexural modulus in the MD direction was measured.
- This reference example is a reference example corresponding to the first embodiment, and is an elliptical circle having a major axis of 28.0 ⁇ m, a minor axis of 7.0 ⁇ m, a major axis / minor axis R of 4.0, and a converted fiber diameter of 15.4 ⁇ m.
- a resin pellet having a glass content C of 40% by mass was prepared in exactly the same manner as in Example 1 except that a chopped strand having a cross-sectional shape and in which glass filaments were focused was used.
- the glass fiber reinforced resin plate (flat plate) created in this reference example was made exactly the same as in Example 1, and the TD direction bending elasticity and the MD direction bending elasticity were measured, and the glass fiber reinforced resin plate was measured. The number average fiber length L of the glass fibers inside was calculated. The results are shown in Table 1.
- Example 4 resin pellets were prepared in exactly the same manner as in Example 1 except that the glass content C was 50% by mass. Next, except that the resin pellets obtained in this example were used, the glass fiber reinforcement was exactly the same as in Example 1, the dimensions were 40 mm in length ⁇ 25 mm in width, and the thickness H was 2.0 mm. A resin plate (flat plate) was created.
- Example 5 In this example, polybutylene terephthalate (manufactured by Polyplastics Co., Ltd., trade name: Juranex 2000, described as PBT in Table 2) was used, except that the glass content C was 30% by mass. Resin pellets were prepared in exactly the same manner as in 1. Next, using the resin pellets obtained in this example, the dimensions are exactly the same as in Example 1 except that the mold temperature is 90 ° C. and the injection temperature is 250 ° C., and the dimensions are 40 mm in length ⁇ 25 mm in width, and the thickness is high. A glass fiber reinforced resin plate (flat plate) having an H of 2.0 mm was prepared.
- Reference Example 8 This reference example is a reference example corresponding to Comparative Example 2, and the resin pellets were prepared in exactly the same manner as in Reference Example 1 except that the glass content C was 10% by mass. Next, except that the resin pellets obtained in this reference example were used, the glass fiber reinforcement was exactly the same as in Example 1, the dimensions were 40 mm in length ⁇ 25 mm in width, and the thickness H was 2.0 mm. A resin plate (flat plate) was created.
- the glass fiber reinforced resin plate (flat plate) produced in this comparative example was made exactly the same as in Example 1, and the TD direction bending elasticity and the MD direction bending elasticity were measured, and the glass fiber reinforced resin plate was measured.
- the number average fiber length L of the glass fibers inside was calculated.
- the total light transmittance was measured by the method described below. The results are shown in Table 3.
- This reference example is a reference example corresponding to Comparative Example 4, in which a polycarbonate PC (manufactured by Teijin Limited, trade name: Panlite L-1250Y, described as PC in Table 3) is used to determine the glass content C.
- Resin pellets were prepared in exactly the same manner as in Reference Example 1 except that the content was 20% by mass.
- the dimensions were exactly the same as in Example 1 except that the mold temperature was 110 ° C. and the injection temperature was 290 ° C., and the dimensions were 20 mm in length ⁇ 25 mm in width, and the thickness was A glass fiber reinforced resin plate (flat plate) having an H of 1.0 mm was prepared.
- the glass fiber reinforced resin plate (flat plate) prepared in this reference example was made exactly the same as in Comparative Example 4, and the TD direction bending elasticity, the MD direction bending elasticity, and the total light transmission rate were measured.
- the number average fiber length L of the glass fibers in the glass fiber reinforced resin plate was calculated. The results are shown in Table 3.
Landscapes
- Chemical & Material Sciences (AREA)
- Health & Medical Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Medicinal Chemistry (AREA)
- Polymers & Plastics (AREA)
- Organic Chemistry (AREA)
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Materials Engineering (AREA)
- Inorganic Chemistry (AREA)
- Compositions Of Macromolecular Compounds (AREA)
- Reinforced Plastic Materials (AREA)
Abstract
TD方向の弾性率が向上した、扁平な断面形状を備えるガラス繊維を含むガラス繊維強化樹脂板を提供する。ガラス繊維強化樹脂板は、扁平な断面形状を備えるガラス繊維と樹脂とを含み、扁平な断面形状を備えるガラス繊維は、短径が4.5~10.5μm、長径が22.0~80.0μm、短径に対する長径の比(長径/短径)Rが4.5~10.0の範囲にあり、ガラス繊維含有率Cが、5.0~75.0質量%、厚さHが0.5mm超10.0mm以下の範囲にあり、前記C及びHが下記式(1)を満たす。 30.0≦H×C≦120.0 ・・・(1)
Description
本発明は、ガラス繊維強化樹脂板に関する。
扁平な断面形状を備えるガラス繊維を含むガラス繊維強化樹脂成形品は、円形断面を備えるガラス繊維を含むガラス繊維強化樹脂成形品よりも、反りの発生が抑制され、寸法安定性に優れるため、携帯電子機器筐体等の軽薄短小な材料に広く用いられている(例えば、特許文献1参照)。
一方、近年、自動車用途を中心に、金属と、板状の繊維強化樹脂成形品との複合材料に注目が集まっている(例えば、特許文献2参照)。
扁平な断面形状を備えるガラス繊維を含むガラス繊維強化樹脂板は、寸法安定性に優れることに加えて、円形断面を備えるガラス繊維を含むガラス繊維強化樹脂板よりも、高い機械的強度を備えるため、金属との複合材料用途にも使用することができると考えられる。
しかしながら、従来使用されてきた、携帯電子機器筐体等の軽薄短小な材料よりも厚く、金属と繊維強化樹脂成形品との複合材料に扁平な断面形状を備えるガラス繊維を含むガラス繊維強化樹脂板が用いられた場合、該ガラス繊維強化樹脂板のTD方向の弾性率が不十分であるという不都合がある。
前記ガラス繊維強化樹脂板のTD方向の弾性率が不十分であると、TD方向の弾性率とMD方向の弾性率とに不均衡が生じ、この不均衡に起因して、金属とガラス繊維強化樹脂板との接着性が低下する。なお、TD方向とは、ガラス繊維を含む樹脂組成物を成形してガラス繊維強化樹脂板を製造する場合に、樹脂組成物が流動する方向と直交する方向を指す。また、MD方向とは、ガラス繊維を含む樹脂組成物を成形してガラス繊維強化樹脂板を製造する場合に、樹脂組成物が流動する方向を指す。
そこで、本発明は、かかる不都合を解消して、扁平な断面形状を備えるガラス繊維を含み、TD方向の弾性率が向上した、ガラス繊維強化樹脂板を提供することにある。
かかる目的を達成するために、本発明は、扁平な断面形状を備えるガラス繊維と樹脂とを含むガラス繊維強化樹脂板であって、前記扁平な断面形状を備えるガラス繊維は、短径が4.5~10.5μmの範囲にあり、長径が22.0~80.0μmの範囲にあり、前記短径に対する長径の比(長径/短径)Rが4.5~10.0の範囲にあり、前記ガラス繊維強化樹脂板におけるガラス繊維含有率Cが、5.0~75.0質量%の範囲にあり、前記ガラス繊維強化樹脂板の厚さHが0.5mm超10.0mm以下の範囲にあり、前記C及びHが下記式(1)を満たすことを特徴とする。
30.0≦H×C≦120.0 ・・・(1)
本発明のガラス繊維強化樹脂板は、扁平な断面形状を備えるガラス繊維と樹脂とを含む。ここで、前記扁平な断面形状を備えるガラス繊維は、短径が4.5~10.5μmの範囲にあり、長径が22.0~80.0μmの範囲にあり、前記短径に対する長径の比(長径/短径)Rが4.5~10.0の範囲にある。
本発明のガラス繊維強化樹脂板は、扁平な断面形状を備えるガラス繊維と樹脂とを含む。ここで、前記扁平な断面形状を備えるガラス繊維は、短径が4.5~10.5μmの範囲にあり、長径が22.0~80.0μmの範囲にあり、前記短径に対する長径の比(長径/短径)Rが4.5~10.0の範囲にある。
前記扁平な断面形状を備えるガラス繊維を含むガラス繊維強化樹脂板では、TD方向の弾性率が不十分になるために、TD方向の弾性率とMD方向の弾性率とに不均衡が生じ、この不均衡に起因して、金属との接着性が低下することが懸念される。
しかし、本発明のガラス繊維強化樹脂板は、ガラス繊維含有率Cが、5.0~75.0質量%の範囲にあり、厚さHが0.5mm超10.0mm以下の範囲にあり、前記C及びHが下記式(1)を満たすことにより、TD方向の弾性率を向上させることができる。ここで、TD方向の弾性率を向上させることができるとは、本発明のガラス繊維強化樹脂板のTD方向の弾性率と、比較対象のガラス繊維強化樹脂板のTD方向の弾性率とを比較して、TD方向の弾性率が5.0%以上向上していることを意味する。前記比較対象のガラス繊維強化樹脂板は、本発明のガラス繊維強化樹脂板に用いられるガラス繊維と同一の断面積を備え、短径に対する長径の比(長径/短径)Rが4.0である扁平な断面形状を備えるガラス繊維を用い、ガラス繊維含有率C及び厚さHを本発明のガラス繊維強化樹脂板と同一とし、本発明のガラス繊維強化樹脂板と同一の成形条件で製造されたガラス繊維強化樹脂板である。
30.0≦H×C≦120.0 ・・・(1)
本発明のガラス繊維強化樹脂板は、ガラス繊維含有率C及び厚さHが前記範囲にあるときに、前記C及びHの積が30.0未満又は120.0超ではTD方向の弾性率を向上させることができない。
本発明のガラス繊維強化樹脂板は、ガラス繊維含有率C及び厚さHが前記範囲にあるときに、前記C及びHの積が30.0未満又は120.0超ではTD方向の弾性率を向上させることができない。
本発明のガラス繊維強化樹脂板は、前記ガラス繊維含有率Cが、20.0~60.0質量%の範囲にあり、前記ガラス繊維強化樹脂板の厚さHが、0.8~8.0mmの範囲にあり、前記C及びHが下記式(2)を満たすことが好ましい。本発明のガラス繊維強化樹脂板は、前記C及びHが前述の範囲にあり、かつ、下記式(2)を満たすことにより、TD方向の弾性率をより向上させることができる。ここで、TD方向の弾性率をより向上させることができるとは、本発明のガラス繊維強化樹脂板のTD方向の弾性率と、前記比較対象のガラス繊維強化樹脂板のTD方向の弾性率とを比較して、TD方向の弾性率が10.0%以上向上していることを意味する。
45.0≦H×C≦80.0 ・・・(2)
また、本発明のガラス繊維強化樹脂板は、TD方向の弾性率をより向上させるために、前記ガラス繊維含有率Cが、20.0~40.0質量%の範囲にあり、前記ガラス繊維強化樹脂板の厚さHが、1.6~5.0mmの範囲にあり、前記C及びHが下記式(3)を満たすことがさらに好ましい。
また、本発明のガラス繊維強化樹脂板は、TD方向の弾性率をより向上させるために、前記ガラス繊維含有率Cが、20.0~40.0質量%の範囲にあり、前記ガラス繊維強化樹脂板の厚さHが、1.6~5.0mmの範囲にあり、前記C及びHが下記式(3)を満たすことがさらに好ましい。
55.0≦H×C≦74.5 ・・・(3)
また、本発明のガラス繊維強化樹脂板は、TD方向の弾性率を向上させるために、前記ガラス繊維強化樹脂板に含まれる樹脂が、結晶性熱可塑性樹脂であることが好ましく、ポリアミドであることがさらに好ましい。
また、本発明のガラス繊維強化樹脂板は、TD方向の弾性率を向上させるために、前記ガラス繊維強化樹脂板に含まれる樹脂が、結晶性熱可塑性樹脂であることが好ましく、ポリアミドであることがさらに好ましい。
次に、本発明の実施の形態についてさらに詳しく説明する。
本実施形態のガラス繊維強化樹脂板は、扁平な断面形状を備えるガラス繊維と、樹脂とを含む成形品である。
本実施形態のガラス繊維強化樹脂板において、前記ガラス繊維を形成するガラスのガラス組成は特に限定されない。本実施形態のガラス繊維強化樹脂板において、ガラス繊維がとりうるガラス組成としては、最も汎用的であるEガラス組成、高強度高弾性率ガラス組成、高弾性率易製造性ガラス組成及び、低誘電率低誘電正接ガラス組成を挙げることができる。
前記Eガラス組成は、ガラス繊維の全量に対し52.0~56.0質量%の範囲のSiO2と、12.0~16.0質量%の範囲のAl2O3と、合計で20.0~25.0質量%の範囲のMgO及びCaOと、5.0~10.0質量%の範囲とB2O3とを含む組成である。
また、前記高強度高弾性率ガラス組成は、ガラス繊維の全量に対し60.0~70.0質量%の範囲のSiO2と、20.0~30.0質量%の範囲のAl2O3と、5.0~15.0質量%の範囲のMgOと、0~1.5質量%のFe2O3と、合計0~0.2質量%の範囲のNa2O、K2O及びLi2Oとを含む組成である。
また、前記高弾性率易製造性ガラス組成は、ガラス繊維の全量に対し57.0~60.0質量%の範囲のSiO2と、17.5~20.0質量%の範囲のAl2O3と、8.5~12.0質量%の範囲のMgOと、10.0~13.0質量%の範囲のCaOと、0.5~1.5質量%の範囲のB2O3とを含み、かつ、SiO2、Al2O3、MgO及びCaOの合計量が98.0質量%以上である組成である。
また、前記低誘電率低誘電正接ガラス組成は、ガラス繊維全量に対し48.0~62.0質量%の範囲のSiO2と、17.0~26.0質量%の範囲のB2O3と、9.0~18.0質量%の範囲のAl2O3と、0.1~9.0質量%の範囲のCaOと、0~6.0質量%の範囲のMgOと、合計で0.05~0.5質量%の範囲のNa2O、K2O及びLi2Oと、0~5.0質量%の範囲のTiO2と、0~6.0質量%の範囲のSrOと、合計で0~3.0質量%の範囲のF2及びCl2と、0~6.0質量%の範囲のP2O5とを含む組成である。
ガラス繊維のガラス組成は、ガラス繊維強化樹脂板の強度を向上させるという観点からは、前記高強度高弾性率ガラス組成、又は、高弾性率易製造性ガラス組成であることが好ましい。また、ガラス繊維のガラス組成は、ガラス繊維強化樹脂板の誘電率および誘電正接を低下させて、ガラス繊維強化樹脂板を通過する高周波信号の伝送損失を低減させるという観点からは、前記低誘電低誘電正接ガラス組成であることが好ましい。
前述したガラスの組成の各成分の含有量の測定は、軽元素であるLiについてはICP発光分光分析装置を用いて、その他の元素は波長分散型蛍光X線分析装置を用いて行うことができる。測定方法としては、次の方法がある。
まず、ガラス繊維を適宜の大きさに裁断した後、白金ルツボに入れ、電気炉中で1550℃の温度に6時間保持して撹拌を加えながら溶融させることにより、均質な溶融ガラスを得る。次に、得られた溶融ガラスをカーボン板上に流し出してガラスカレットを作製した後、粉砕し粉末化して、ガラス粉末を得る。
軽元素であるLiについては前記ガラス粉末を酸で加熱分解した後、ICP発光分光分析装置を用いて定量分析する。その他の元素は前記ガラス粉末をプレス機で円盤状に成形した後、波長分散型蛍光X線分析装置を用いて定量分析する。これらの定量分析結果を酸化物換算して各成分の含有量及び全量を計算し、これらの数値から前述した各成分の含有量(質量%)を求めることができる。
前記ガラス繊維は、ガラス繊維表面に有機物が付着している場合、又は、ガラス繊維が有機物(樹脂)中に主に強化材として含まれている場合には、例えば、300~650℃のマッフル炉で2~24時間程度加熱する等して、有機物を除去してから用いる。
前述のガラス組成を備えるガラス繊維は、以下のようにして製造することができる。初めに、前述の組成となるように調合されたガラス原料(ガラスバッチ)を溶融炉に供給し、例えば、1450~1550℃の範囲の温度で溶融する。次に、溶融されたガラスバッチ(溶融ガラス)を所定の温度に制御された、ブッシングの1~30000個のノズルチップから引き出して、急冷することで、ガラスフィラメントを形成する。次に、形成されたガラスフィラメントに、塗布装置であるアプリケーターを用いて集束剤又はバインダーを塗布し、集束シューを用いて、ガラスフィラメント1~30000本を集束させながら、巻取り機を用いて、チューブに高速で巻取ることで、ガラス繊維を得ることができる。
ここで、本実施形態のガラス繊維強化樹脂板に用いる、扁平な断面形状を備えるガラス繊維は、前記ノズルチップを、非円形形状を有し、溶融ガラスを急冷する突起部や切欠部を有するものとし、温度条件を制御することにより得ることができる。また、ノズルチップの径や、巻取り速度、及び、温度条件等を調整することで、ガラス繊維の短径及び長径を調整することができる。例えば、巻取り速度を速くすることで、短径及び長径を小さくすることができ、巻取り速度を遅くすることで、短径及び長径を大きくすることができる。
本実施形態のガラス繊維強化樹脂板に用いる、扁平な断面形状を備えるガラス繊維は、短径が4.5~10.5μm、好ましくは5.0~8.0μm、より好ましくは5.0~6.4μmの範囲にあり、長径が22.0~80.0μm、好ましくは28.5~70.0μm、より好ましくは29.5~65.0μm、さらに好ましくは32.5~60.0μm、特に好ましくは32.5~50.0μmの範囲にあり、前記短径に対する長径の比(長径/短径)Rが4.5~10.0、好ましくは5.0~7.9、より好ましくは5.0~6.7、さらに好ましくは5.5~6.5の範囲にある。また、前記扁平な断面形状とは、好ましくは楕円形状又は長円形状であり、より好ましくは長円形状である。前記長円形状とは、長方形の両端に半円状の形状を付けたもの、あるいはそれに類似した形状である。
本実施形態のガラス繊維強化樹脂板に用いる、扁平な断面形状を備えるガラス繊維の換算繊維径は、11.0~32.0μmの範囲にあり、好ましくは、12.0~22.0μmの範囲にあり、より好ましくは、12.5~20.0μmの範囲にあり、さらに好ましくは、13.5~18.0μmの範囲にある。ここで、換算繊維径とは、扁平な断面形状を備えるガラス繊維の断面積と同一の断面積を有し、円形断面を備えるガラス繊維の直径を意味する。
本実施形態のガラス繊維強化樹脂板における、扁平な断面形状を備えるガラス繊維の短径及び長径は、例えば、次のようにして算出することができる。
まず、ガラス繊維強化樹脂板の断面を研磨する。次いで、電子顕微鏡を用いて、ガラスフィラメント100本以上につき、ガラスフィラメント断面の略中心を通る最長の辺を長径とし、該長径とガラスフィラメント断面の略中心で直交する辺を短径として、それぞれの長さを測定する。そして、前記短径と長径とについて、それぞれの長さの測定値の平均値を求めることで、ガラス繊維の短径及び長径を算出することができる。
なお、ガラス繊維は、通常、複数本のガラスフィラメントが集束されて形成されているが、ガラス繊維強化樹脂板においては、成形加工を経ることにより前記集束が解かれ、ガラスフィラメントの状態で、ガラス繊維強化樹脂板中に分散して存在している。
ここで、本実施形態のガラス繊維強化樹脂板における、扁平な断面形状を備えるガラス繊維が成形加工前にとる好ましい形態としては、ガラス繊維を構成するガラスフィラメントの本数(集束本数)が好ましくは1~20000本、より好ましくは50~10000本、さらに好ましくは1000~8000本の範囲であり、ガラス繊維(ガラス繊維束又はガラスストランドともいう)の長さを好ましくは1.0~100.0mm、より好ましくは、1.2~51.0mm、さらに好ましくは、1.5~30.0mm、特に好ましくは2.0~15.0mm、最も好ましくは2.3~7.8mmの範囲に切断したチョップドストランドを挙げることができる。また、本実施形態のガラス繊維強化樹脂板における、扁平な断面形状を備えるガラス繊維が成形加工前にとりうる形態としては、チョップドストランド以外に、例えば、ガラス繊維を構成するガラスフィラメントの本数が10~30000本の範囲で、切断を行わない、ロービングや、ガラス繊維を構成するガラスフィラメントの本数が1~20000本の範囲で、ボールミル又はヘンシルミキサー等の公知の方法により長さ0.001~0.900mmの範囲になるように粉砕した、カットファイバーを挙げることができる。
本実施形態のガラス繊維強化樹脂板において、ガラス繊維は、ガラス繊維と樹脂との接着性の向上、ガラス繊維と樹脂又は無機材料との混合物中におけるガラス繊維の均一分散性の向上等を目的として、その表面を有機物で被覆されてもよい。このような有機物としては、樹脂、又は、シランカップリング剤、及び、これらに加えて潤滑剤、界面活性剤等を含む組成物を挙げることができる。ここで、前記組成物は、樹脂及びシランカップリング剤を含んでもよい。
このような組成物は、組成物に被覆されていない状態における、ガラス繊維の質量を基準として、0.1~2.0質量%の範囲の割合で、ガラス繊維を被覆する。
前記樹脂としては、ウレタン樹脂、エポキシ樹脂、酢酸ビニル樹脂、アクリル樹脂、変性ポリプロピレン、特にカルボン酸変性ポリプロピレン、(ポリ)カルボン酸、特にマレイン酸と不飽和単量体との共重合体等を挙げることができる。
なお、有機物によるガラス繊維の被覆は、例えば、ガラス繊維の製造工程において、ローラー型アプリケーター等の公知の方法を用いて、前記組成物、前記樹脂、又は、前記シランカップリング剤の溶液を含む前記集束剤又はバインダーをガラス繊維に塗布し、その後、前記樹脂、前記シランカップリング剤又は前記組成物の塗布されたガラス繊維を乾燥させることで行うことができる。
ここで、シランカップリング剤としては、アミノシラン、クロルシラン、エポキシシラン、メルカプトシラン、ビニルシラン、アクリルシラン、カチオニックシランを挙げることができる。前記シランカップリング剤は、これらの化合物を単独で使用することもでき、又は、2種類以上を併用することもできる。
前記アミノシランとしては、γ-アミノプロピルトリエトキシシラン、N-β-(アミノエチル)-γ-アミノプロピルトリメトキシシラン、N-β-(アミノエチル)-N’-β-(アミノエチル)-γ-アミノプロピルトリメトキシシラン、γ-アニリノプロピルトリメトキシシラン等を挙げることができる。
また、前記クロルシランとしては、γ-クロロプロピルトリメトキシシラン等を挙げることができる。
また、前記エポキシシランとしては、γ-グリシドキシプロピルトリメトキシシラン、β-(3,4-エポキシシクロヘキシル)エチルトリメトキシシラン等を挙げることができる。
また、前記メルカプトシランとしては、γ-メルカプトトリメトキシシラン等を挙げることができる。
また、前記ビニルシランとしては、ビニルトリメトキシシラン、N-β-(N-ビニルベンジルアミノエチル)-γ-アミノプロピルトリメトキシシラン等を挙げることができる。
また、前記アクリルシランとしては、γ-メタクリロキシプロピルトリメトキシシラン等を挙げることができる。
また、前記カチオニックシランとしては、N-(ビニルベンジル)-2-アミノエチル-3-アミノプロピルトリメトキシシラン塩酸塩、N-フェニル-3-アミノプロピルトリメトキシシラン塩酸塩等を挙げることができる。
潤滑剤としては、変性シリコーンオイル、動物油及びこの水素添加物、植物油及びこの水素添加物、動物性ワックス、植物性ワックス、鉱物系ワックス、高級飽和脂肪酸と高級飽和アルコールとの縮合物、ポリエチレンイミン、ポリアルキルポリアミンアルキルアマイド誘導体、脂肪酸アミド、第4級アンモニウム塩を挙げることができる。前記潤滑剤は、これらを単独で使用することもでき、又は、2種類以上を併用することもできる。
前記動物油としては、牛脂等を挙げることができる。
また、前記植物油としては、大豆油、ヤシ油、ナタネ油、パーム油、ひまし油等を挙げることができる。また、前記動物性ワックスとしては、蜜蝋、ラノリン等を挙げることができる。また、前記植物性ワックスとしては、キャンデリラワックス、カルナバワックス等を挙げることができる。
また、前記鉱物系ワックスとしては、パラフィンワックス、モンタンワックス等を挙げることができる。また、前記高級飽和脂肪酸と高級飽和アルコールとの縮合物としては、ラウリルステアレート等のステアリン酸エステル等を挙げることができる。
また、前記脂肪酸アミドとしては、ジエチレントリアミン、トリエチレンテトラミン、テトラエチレンペンタミン等のポリエチレンポリアミンと、ラウリン酸、ミリスチン酸、パルミチン酸、ステアリン酸等の脂肪酸との脱水縮合物等を挙げることができる。
また、前記第4級アンモニウム塩としては、ラウリルトリメチルアンモニウムクロライド等のアルキルトリメチルアンモニウム塩等を挙げることができる。
界面活性剤としては、ノニオン系界面活性剤、カチオン系界面活性剤、アニオン系界面活性剤、両性界面活性剤を挙げることができる。前記界面活性剤は、これらを単独で使用することもでき、又は、2種類以上を併用することもできる。
ノニオン系界面活性剤としては、エチレンオキサイドプロピレンオキサイドアルキルエーテル、ポリオキシエチレンアルキルエーテル、ポリオキシエチレン-ポリオキシプロピレン-ブロックコポリマー、アルキルポリオキシエチレン-ポリオキシプロピレン-ブロックコポリマーエーテル、ポリオキシエチレン脂肪酸エステル、ポリオキシエチレン脂肪酸モノエステル、ポリオキシエチレン脂肪酸ジエステル、ポリオキシエチレンソルビタン脂肪酸エステル、グリセロール脂肪酸エステルエチレンオキサイド付加物、ポリオキシエチレンキャスターオイルエーテル、硬化ヒマシ油エチレンオキサイド付加物、アルキルアミンエチレンオキサイド付加物、脂肪酸アミドエチレンオキサイド付加物、グリセロール脂肪酸エステル、ポリグリセリン脂肪酸エステル、ペンタエリスリトール脂肪酸エステル、ソルビトール脂肪酸エステル、ソルビタン脂肪酸エステル、ショ糖脂肪酸エステル、多価アルコールアルキルエーテル、脂肪酸アルカノールアミド、アセチレングリコール、アセチレンアルコール、アセチレングリコールのエチレンオキサイド付加物、アセチレンアルコールのエチレンオキサイド付加物等を挙げることができる。
カチオン系界面活性剤としては、塩化アルキルジメチルベンジルアンモニウム、塩化アルキルトリメチルアンモニウム、アルキルジメチルエチルアンモニウムエチルサルフェート、高級アルキルアミン塩(酢酸塩や塩酸塩等)、高級アルキルアミンへのエチレンオキサイド付加物、高級脂肪酸とポリアルキレンポリアミンとの縮合物、高級脂肪酸とアルカノールアミンとのエステルの塩、高級脂肪酸アミドの塩、イミダゾリン型カチオン性界面活性剤、アルキルピリジニウム塩等を挙げることができる。
アニオン系界面活性剤としては、高級アルコール硫酸エステル塩、高級アルキルエーテル硫酸エステル塩、α-オレフィン硫酸エステル塩、アルキルベンゼンスルホン酸塩、α-オレフィンスルホン酸塩、脂肪酸ハライドとN-メチルタウリンとの反応生成物、スルホコハク酸ジアルキルエステル塩、高級アルコールリン酸エステル塩、高級アルコールエチレンオキサイド付加物のリン酸エステル塩等を挙げることができる。
両性界面活性剤としては、アルキルアミノプロピオン酸アルカリ金属塩等のアミノ酸型両性界面活性剤、アルキルジメチルベタイン等のベタイン型、イミダゾリン型両性界面活性剤等を挙げることができる。
また、本実施形態のガラス繊維強化樹脂板に用いる樹脂としては、熱可塑性樹脂を挙げることができる。
ここで、前記熱可塑性樹脂としては、ポリエチレン、ポリプロピレン、ポリスチレン、スチレン/無水マレイン酸樹脂、スチレン/マレイミド樹脂、ポリアクリロニトリル、アクリロニトリル/スチレン(AS)樹脂、アクリロニトリル/ブタジエン/スチレン(ABS)樹脂、塩素化ポリエチレン/アクリロニトリル/スチレン(ACS)樹脂、アクリロニトリル/エチレン/スチレン(AES)樹脂、アクリロニトリル/スチレン/アクリル酸メチル(ASA)樹脂、スチレン/アクリロニトリル(SAN)樹脂、メタクリル樹脂、ポリ塩化ビニル(PVC)、ポリ塩化ビニリデン(PVDC)、ポリアミド、ポリアセタール、ポリエチレンテレフタレート(PET)、ポリブチレンテレフタレート(PBT)、ポリトリメチレンテレフタレート(PTT)、ポリカーボネート、ポリアリーレンサルファイド、ポリエーテルスルホン(PES)、ポリフェニルスルホン(PPSU)、ポリフェニレンエーテル(PPE)、変性ポリフェニレンエーテル(m-PPE)、ポリアリールエーテルケトン、液晶ポリマー(LCP)、フッ素樹脂、ポリエーテルイミド(PEI)、ポリアリレート(PAR)、ポリサルフォン(PSF)、ポリアミドイミド(PAI)、ポリアミノビスマレイミド(PABM)、熱可塑性ポリイミド(TPI)、ポリエチレンナフタレート(PEN)、エチレン/酢酸ビニル(EVA)樹脂、アイオノマー(IO)樹脂、ポリブタジエン、スチレン/ブタジエン樹脂、ポリブチレン、ポリメチルペンテン、オレフィン/ビニルアルコール樹脂、環状オレフィン樹脂、セルロース樹脂、ポリ乳酸等を挙げることができる。
具体的に、ポリエチレンとしては、高密度ポリエチレン(HDPE)、中密度ポリエチレン、低密度ポリエチレン(LDPE)、直鎖状低密度ポリエチレン(LLDPE)、超高分子量ポリエチレン等を挙げることができる。
ポリプロピレンとしては、アイソタクチックポリプロピレン、アタクチックポリプロピレン、シンジオタクチックポリプロピレン及びこれらの混合物等を挙げることができる。
ポリスチレンとしては、アタクチック構造を有するアタクチックポリスチレンである汎用ポリスチレン(GPPS)、GPPSにゴム成分を加えた耐衝撃性ポリスチレン(HIPS)、シンジオタクチック構造を有するシンジオタクチックポリスチレン等を挙げることができる。
メタクリル樹脂としては、アクリル酸、メタクリル酸、スチレン、アクリル酸メチル、アクリル酸エチル、メタクリル酸エチル、アクリル酸ブチル、メタクリル酸ブチル、脂肪酸ビニルエステルのうち一種を単独重合した重合体、又は二種以上を共重合した重合体等を挙げることができる。
ポリ塩化ビニルとしては、従来公知の乳化重合法、懸濁重合法、マイクロ懸濁重合法、塊状重合法等の方法により重合される塩化ビニル単独重合体、または、塩化ビニルモノマーと共重合可能なモノマーとの共重合体、または、重合体に塩化ビニルモノマーをグラフト重合したグラフト共重合体等を挙げることができる。
ポリアミドとしては、ポリカプロアミド(ポリアミド6)、ポリヘキサメチレンアジパミド(ポリアミド66)、ポリテトラメチレンアジパミド(ポリアミド46)、ポリテトラメチレンセバカミド(ポリアミド410)、ポリペンタメチレンアジパミド(ポリアミド56)、ポリペンタメチレンセバカミド(ポリアミド510)、ポリヘキサメチレンセバカミド(ポリアミド610)、ポリヘキサメチレンドデカミド(ポリアミド612)、ポリデカメチレンアジパミド(ポリアミド106)、ポリデカメチレンセバカミド(ポリアミド1010)、ポリデカメチレンドデカミド(ポリアミド1012)、ポリウンデカンアミド(ポリアミド11)、ポリウンデカメチレンアジパミド(ポリアミド116)、ポリドデカンアミド(ポリアミド12)、ポリキシレンアジパミド(ポリアミドXD6)、ポリキシレンセバカミド(ポリアミドXD10)、ポリメタキシリレンアジパミド(ポリアミドMXD6)、ポリパラキシリレンアジパミド(ポリアミドPXD6)、ポリテトラメチレンテレフタルアミド(ポリアミド4T)、ポリペンタメチレンテレフタルアミド(ポリアミド5T)、ポリヘキサメチレンテレフタルアミド(ポリアミド6T)、ポリヘキサメチレンイソフタルアミド(ポリアミド6I)、ポリノナメチレンテレフタルアミド(ポリアミド9T)、ポリデカメチレンテレフタルアミド(ポリアミド10T)、ポリウンデカメチレンテレフタルアミド(ポリアミド11T)、ポリドデカメチレンテレフタルアミド(ポリアミド12T)、ポリテトラメチレンイソフタルアミド(ポリアミド4I)、ポリビス(3-メチル-4-アミノヘキシル)メタンテレフタルアミド(ポリアミドPACMT)、ポリビス(3-メチル-4-アミノヘキシル)メタンイソフタルアミド(ポリアミドPACMI)、ポリビス(3-メチル-4-アミノヘキシル)メタンドデカミド(ポリアミドPACM12)、ポリビス(3-メチル-4-アミノヘキシル)メタンテトラデカミド(ポリアミドPACM14)等の成分のうち1種、もしくは2種以上の複数成分を組み合わせた共重合体やこれらの混合物等を挙げることができる。
ポリアセタールとしては、オキシメチレン単位を主たる繰り返し単位とする単独重合体、および、主としてオキシメチレン単位からなり、主鎖中に2~8個の隣接する炭素原子を有するオキシアルキレン単位を含有する共重合体等を挙げることができる。
ポリエチレンテレフタレートとしては、テレフタル酸またはその誘導体と、エチレングリコールを重縮合することにより得られる重合体等を挙げることができる。
ポリブチレンテレフタレートとしては、テレフタル酸またはその誘導体と、1,4-ブタンジオールを重縮合することにより得られる重合体等を挙げることができる。
ポリトリメチレンテレフタレートとしては、テレフタル酸またはその誘導体と、1,3-プロパンジオールを重縮合することにより得られる重合体等を挙げることができる。
ポリカーボネートとしては、ジヒドロキシジアリール化合物とジフェニルカーボネート等の炭酸エステルとを溶融状態で反応させるエステル交換法により得られる重合体、又は、ジヒドロキシアリール化合物とホスゲンとを反応するホスゲン法により得られる重合体を挙げることができる。
ポリアリーレンサルファイドとしては、直鎖型ポリフェニレンサルファイド、重合の後に硬化反応を行うことで高分子量化した架橋型ポリフェニレンサルファイド、ポリフェニレンサルファイドサルフォン、ポリフェニレンサルファイドエーテル、ポリフェニレンサルファイドケトン等を挙げることができる。
ポリフェニレンエーテルとしては、ポリ(2,3-ジメチル-6-エチル-1,4-フェニレンエーテル)、ポリ(2-メチル-6-クロロメチル-1,4-フェニレンエーテル)、ポリ(2-メチル-6-ヒドロキシエチル-1,4-フェニレンエーテル)、ポリ(2-メチル-6-n-ブチル-1,4-フェニレンエーテル)、ポリ(2-エチル-6-イソプロピル-1,4-フェニレンエーテル)、ポリ(2-エチル-6-n-プロピル-1,4-フェニレンエーテル)、ポリ(2,3,6-トリメチル-1,4-フェニレンエーテル)、ポリ〔2-(4’-メチルフェニル)-1,4-フェニレンエーテル〕、ポリ(2-ブロモ-6-フェニル-1,4-フェニレンエーテル)、ポリ(2-メチル-6-フェニル-1,4-フェニレンエーテル)、ポリ(2-フェニル-1,4-フェニレンエーテル)、ポリ(2-クロロ-1,4-フェニレンエーテル)、ポリ(2-メチル-1,4-フェニレンエーテル)、ポリ(2-クロロ-6-エチル-1,4-フェニレンエーテル)、ポリ(2-クロロ-6-ブロモ-1,4-フェニレンエーテル)、ポリ(2,6-ジ-n-プロピル-1,4-フェニレンエーテル)、ポリ(2-メチル-6-イソプロピル-1,4-フェニレンエーテル)、ポリ(2-クロロ-6-メチル-1,4-フェニレンエーテル)、ポリ(2-メチル-6-エチル-1,4-フェニレンエーテル)、ポリ(2,6-ジブロモ-1,4-フェニレンエーテル)、ポリ(2,6-ジクロロ-1,4-フェニレンエーテル)、ポリ(2,6-ジエチル-1,4-フェニレンエーテル)、ポリ(2,6-ジメチル-1,4-フェニレンエーテル)等を挙げることができる。
変性ポリフェニレンエーテルとしては、ポリ(2,6-ジメチル-1,4-フェニレン)エーテルとポリスチレンとのポリマーアロイ、ポリ(2,6-ジメチル-1,4-フェニレン)エーテルとスチレン/ブタジエン共重合体とのポリマーアロイ、ポリ(2,6-ジメチル-1,4-フェニレン)エーテルとスチレン/無水マレイン酸共重合体とのポリマーアロイ、ポリ(2,6-ジメチル-1,4-フェニレン)エーテルとポリアミドとのポリマーアロイ、ポリ(2,6-ジメチル-1,4-フェニレン)エーテルとスチレン/ブタジエン/アクリロニトリル共重合体とのポリマーアロイ、前記ポリフェニレンエーテルのポリマー鎖末端にアミノ基、エポキシ基、カルボキシ基、スチリル基等の官能基を導入したもの、前記ポリフェニレンエーテルのポリマー鎖側鎖にアミノ基、エポキシ基、カルボキシ基、スチリル基、メタクリル基等の官能基を導入したもの等を挙げることができる。
ポリアリールエーテルケトンとしては、ポリエーテルケトン(PEK)、ポリエーテルエーテルケトン(PEEK)、ポリエーテルケトンケトン(PEKK)、ポリエーテルエーテルケトンケトン(PEEKK)等を挙げることができる。
液晶ポリマー(LCP)としては、サーモトロピック液晶ポリエステルである芳香族ヒドロキシカルボニル単位、芳香族ジヒドロキシ単位、芳香族ジカルボニル単位、脂肪族ジヒドロキシ単位、脂肪族ジカルボニル単位等から選ばれる1種以上の構造単位からなる(共)重合体等を挙げることができる。
フッ素樹脂としては、ポリテトラフルオロエチレン(PTFE)、パーフルオロアルコキシ樹脂(PFA)、フッ化エチレンプロピレン樹脂(FEP)、フッ化エチレンテトラフルオロエチレン樹脂(ETFE)、ポリビニルフロライド(PVF)、ポリフッ化ビニリデン(PVDF)、ポリクロロトリフルオロエチレン(PCTFE)、エチレン/クロロトリフルオロエチレン樹脂(ECTFE)等を挙げることができる。
アイオノマー(IO)樹脂としては、オレフィンまたはスチレンと不飽和カルボン酸との共重合体であって、カルボキシル基の一部を金属イオンで中和してなる重合体等を挙げることができる。
オレフィン/ビニルアルコール樹脂としては、エチレン/ビニルアルコール共重合体、プロピレン/ビニルアルコール共重合体、エチレン/酢酸ビニル共重合体ケン化物、プロピレン/酢酸ビニル共重合体ケン化物等を挙げることができる。
環状オレフィン樹脂としては、シクロヘキセン等の単環体、テトラシクロペンタジエン等の多環体、環状オレフィンモノマーの重合体等を挙げることができる。
ポリ乳酸としては、L体の単独重合体であるポリL-乳酸、D体の単独重合体であるポリD-乳酸、またはその混合物であるステレオコンプレックス型ポリ乳酸等を挙げることができる。
セルロース樹脂としては、メチルセルロース、エチルセルロース、ヒドロキシセルロース、ヒドロキシメチルセルロース、ヒドロキシエチルセルロース、ヒドロキシエチルメチルセルロース、ヒドロキシプロピルメチルセルロース、セルロースアセテート、セルロースプロピオネート、セルロースブチレート等を挙げることができる。
本実施形態のガラス繊維強化樹脂板に用いる樹脂は、TD方向の弾性率の向上効果が大きくなることから、好ましくは結晶性熱可塑性樹脂である。前記結晶性熱可塑性樹脂としては、ポリアミド、ポリブチレンテレフタレート、ポリフェニレンサルファイド、ポリエーテルエーテルケトン、ポリエチレン、ポリプロピレン等を挙げることができるが、さらに好ましくはポリアミドであり、特に好ましくはポリアミド6である。
また、本実施形態のガラス繊維強化樹脂板に用いる樹脂は、前記結晶性熱可塑性樹脂である場合、非晶性熱可塑性樹脂を含まないことが好ましい。
本実施形態のガラス繊維強化樹脂板に用いる樹脂が透明樹脂である場合、本実施形態のガラス繊維強化樹脂板は、比較対象のガラス繊維強化樹脂板に対して、可視光線、紫外線、赤外線、レーザー光線等の光線透過率を向上させることができる。前記比較対象のガラス繊維強化樹脂板は、本実施形態のガラス繊維強化樹脂板に用いられるガラス繊維と同一の断面積を備え、短径に対する長径の比(長径/短径)Rが4.0である扁平な断面形状を備えるガラス繊維を用い、ガラス繊維含有率C及び厚さHを本実施形態のガラス繊維強化樹脂板と同一とし、本実施形態のガラス繊維強化樹脂板と同一の成形条件で製造されたガラス繊維強化樹脂板である。ここで、前記透明樹脂としては、ポリスチレン、ABS樹脂、(メタ)アクリル樹脂、ポリアセタール、ポリエチレンテレフタレート、ポリカーボネート、及びポリアリレートを挙げることができる。
本実施形態のガラス繊維強化樹脂板は、例えば、前記扁平な断面形状を備えるガラス繊維のガラスフィラメントが集束されてなり、所定の長さを備えるチョップドストランドと、前記樹脂とを、二軸混練機にて混練し、得られた樹脂ペレットを用いて射出成形を行うことにより得ることができる。また、本実施形態のガラス繊維強化樹脂板は、射出圧縮成形法、二色成形法、中空成形法、発泡成形法(超臨界流体発泡成形法含む)、インサート成形法、インモールドコーティング成形法、押出成形法、シート成形法、熱成形法、回転成形法、積層成形法、プレス成形法、ブロー成形法、スタンピング成形法、インフュージョン法、ハンドレイアップ法、スプレイアップ法、レジントランスファーモールディング法、シートモールディングコンパウンド法、バルクモールディングコンパウンド法、プルトルージョン法、フィラメントワインディング法等の公知の成形方法を用いても得ることができる。前述のようにして得られた本実施形態のガラス繊維強化樹脂板の形状は、平板、孔や凹凸を有する平板、又は、曲面や折れ曲がりを有する板であってよい。ここで、曲面や折れ曲がりを有する板の一態様として、中空円筒体、中空多角柱及び箱が含まれる。
本実施形態のガラス繊維強化樹脂板は、ガラス繊維含有率Cが、5.0~75.0質量%の範囲にあり、厚さHが0.5mm超10.0mm以下の範囲にあり、前記C及びHが下記式(1)を満たすことにより、TD方向の弾性率を向上させることができる。
30.0≦H×C≦120.0 ・・・(1)
また、本実施形態のガラス繊維強化樹脂板において、前記ガラス繊維含有率Cは、好ましくは20.0~60.0質量%、さらに好ましくは20.0~40.0質量%、より好ましくは21.0~38.0質量%の範囲にある。また、本実施形態のガラス繊維強化樹脂板において、前記ガラス繊維強化樹脂板の厚さHは、好ましくは0.8~8.0mm、より好ましくは1.6~5.0mm、さらに好ましくは1.6~3.4mm、特に好ましくは1.6~2.4mmの範囲にある。また、本実施形態のガラス繊維強化樹脂板において、前記C及びHは、好ましくは下記式(2)を満たし、より好ましくは下記式(3)を満たし、さらに好ましくは下記式(4)を満たし、特に好ましくは下記式(5)を満たし、とりわけ好ましくは下記式(6)を満たし、最も好ましくは下記式(7)を満たす。
また、本実施形態のガラス繊維強化樹脂板において、前記ガラス繊維含有率Cは、好ましくは20.0~60.0質量%、さらに好ましくは20.0~40.0質量%、より好ましくは21.0~38.0質量%の範囲にある。また、本実施形態のガラス繊維強化樹脂板において、前記ガラス繊維強化樹脂板の厚さHは、好ましくは0.8~8.0mm、より好ましくは1.6~5.0mm、さらに好ましくは1.6~3.4mm、特に好ましくは1.6~2.4mmの範囲にある。また、本実施形態のガラス繊維強化樹脂板において、前記C及びHは、好ましくは下記式(2)を満たし、より好ましくは下記式(3)を満たし、さらに好ましくは下記式(4)を満たし、特に好ましくは下記式(5)を満たし、とりわけ好ましくは下記式(6)を満たし、最も好ましくは下記式(7)を満たす。
45.0≦H×C≦80.0 ・・・(2)
55.0≦H×C≦74.5 ・・・(3)
59.0≦H×C≦72.0 ・・・(4)
59.0≦H×C≦69.0 ・・・(5)
59.0≦H×C≦66.0 ・・・(6)
59.0≦H×C≦64.0 ・・・(7)
また、本実施形態のガラス繊維強化樹脂板に含まれる前記ガラス繊維の数平均繊維長Lは、100~700μm、好ましくは150~450μm、より好ましくは200~400μmの範囲にあり、さらに好ましくは、220~380μmの範囲にある。
55.0≦H×C≦74.5 ・・・(3)
59.0≦H×C≦72.0 ・・・(4)
59.0≦H×C≦69.0 ・・・(5)
59.0≦H×C≦66.0 ・・・(6)
59.0≦H×C≦64.0 ・・・(7)
また、本実施形態のガラス繊維強化樹脂板に含まれる前記ガラス繊維の数平均繊維長Lは、100~700μm、好ましくは150~450μm、より好ましくは200~400μmの範囲にあり、さらに好ましくは、220~380μmの範囲にある。
ここで、本実施形態のガラス繊維強化樹脂板に含まれる前記ガラス繊維の数平均繊維長Lは、本実施形態のガラス繊維強化樹脂板を射出成形による得る場合、例えば、二軸混練機に投入されるチョップドストランドの長さ、二軸混練機のスクリュー回転数を調整することにより制御することができる。例えば、二軸混練機に投入されるチョップドストランドの長さを、1.0~100.0mmの範囲で長くすることにより、前記Lを長くするこができ、チョップドストランドの長さを短くすることで、前記Lを短くすることができる。また、二軸混練時のスクリュー回転数を10~1000rpmの範囲で低くすることで、前記Lを長くすることができ、回転数を高くすることで、前記Lを短くすることができる。
ここで、ガラス繊維含有率C、ガラス繊維強化樹脂板の厚さH及びガラス繊維の数平均繊維長Lは、好ましくは下記式(a)を満たし、より好ましくは下記式(b)を満たし、さらに好ましくは下記式(c)を満たし、特に好ましくは下記式(d)を満たし、最も好ましくは下記式(e)を満たす。
0.31≦(C/L)(1/2)×H≦1.01 ・・・(a)
0.41≦(C/L)(1/2)×H≦0.71 ・・・(b)
0.46≦(C/L)(1/2)×H≦0.71 ・・・(c)
0.51≦(C/L)(1/2)×H≦0.71 ・・・(d)
0.56≦(C/L)(1/2)×H≦0.66 ・・・(e)
本実施形態のガラス繊維強化樹脂板の用途としては、自動車の板状金属代替材料、自動車用途の金属と板状の繊維強化樹脂成形品との複合材料を挙げることができるが、これらに限定されない。本実施形態のガラス繊維強化樹脂板は、例えば、フロントフェンダー、ドアパネル等の自動車外装部品、トリム、グローブボックス等の自動車内装部品、シリンダーヘッドカバー、ラジエータータンク等の自動車ギア部品等に好ましく用いることができる。
次に、本発明の実施例、比較例及び参考例を示す。
〔実施例1〕
本実施例では、長径が34.1μm、短径が5.7μm、長径/短径Rが6.0、換算繊維径が15.4μmである長円形状の断面形状を備え、Eガラス組成である、ガラスフィラメントが集束されてなり、シランカップリング剤組成物で被覆された、50mmの長さを備えるチョップドストランドと、ポリアミド6(宇部興産株式会社製、商品名:UBEナイロン1015B、表1中、PAと記載する)とを、スクリュー回転数を100rpmとして、二軸混練機(芝浦機械株式会社製、商品名:TEM-26SS)にて混練し、ガラス含有率Cが40質量%の樹脂ペレットを作製した。
本実施例では、長径が34.1μm、短径が5.7μm、長径/短径Rが6.0、換算繊維径が15.4μmである長円形状の断面形状を備え、Eガラス組成である、ガラスフィラメントが集束されてなり、シランカップリング剤組成物で被覆された、50mmの長さを備えるチョップドストランドと、ポリアミド6(宇部興産株式会社製、商品名:UBEナイロン1015B、表1中、PAと記載する)とを、スクリュー回転数を100rpmとして、二軸混練機(芝浦機械株式会社製、商品名:TEM-26SS)にて混練し、ガラス含有率Cが40質量%の樹脂ペレットを作製した。
次に、本実施例で得られた樹脂ペレットを用い、射出成形機(日精樹脂工業株式会社製、商品名:NEX80)により金型温度90℃、射出温度270℃にて射出成形を行い、寸法が縦80mm×横60mmであり、厚さHが1.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本実施例で作成したガラス繊維強化樹脂板(平板)について、以下に述べる方法で、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表1に示す。
[TD方向曲げ弾性率]
ガラス繊維強化樹脂板を、試験片の長さ方向が、該ガラス繊維強化樹脂板のTD方向に相当し、試験片の幅方向が、該ガラス繊維強化樹脂板のMD方向に相当するように、幅25mm×長さ20mmに加工して、試験片を得た。次いで、得られた試験片について、試験温度23℃の条件で、精密万能試験機(株式会社島津製作所製、商品名:オートグラフAG-XPlus)を用いて、JIS K 7171:2016に準拠した静的曲げ試験を行い、TD方向曲げ弾性率を測定した。
ガラス繊維強化樹脂板を、試験片の長さ方向が、該ガラス繊維強化樹脂板のTD方向に相当し、試験片の幅方向が、該ガラス繊維強化樹脂板のMD方向に相当するように、幅25mm×長さ20mmに加工して、試験片を得た。次いで、得られた試験片について、試験温度23℃の条件で、精密万能試験機(株式会社島津製作所製、商品名:オートグラフAG-XPlus)を用いて、JIS K 7171:2016に準拠した静的曲げ試験を行い、TD方向曲げ弾性率を測定した。
[MD方向曲げ弾性率]
ガラス繊維強化樹脂板を、試験片の長さ方向が、該ガラス繊維強化樹脂板のMD方向に相当し、試験片の幅方向が、該ガラス繊維強化樹脂板のTD方向に相当するように、幅25mm×長さ20mmに加工して、試験片を得た。次いで、得られた試験片について、試験温度23℃の条件で、精密万能試験機(株式会社島津製作所製、商品名:オートグラフAG-XPlus)を用いて、JIS K 7171:2016に準拠した静的曲げ試験を行い、MD方向曲げ弾性率を測定した。
ガラス繊維強化樹脂板を、試験片の長さ方向が、該ガラス繊維強化樹脂板のMD方向に相当し、試験片の幅方向が、該ガラス繊維強化樹脂板のTD方向に相当するように、幅25mm×長さ20mmに加工して、試験片を得た。次いで、得られた試験片について、試験温度23℃の条件で、精密万能試験機(株式会社島津製作所製、商品名:オートグラフAG-XPlus)を用いて、JIS K 7171:2016に準拠した静的曲げ試験を行い、MD方向曲げ弾性率を測定した。
[ガラス繊維の数平均繊維長L]
ガラス繊維強化樹脂板における、ガラス繊維の数平均繊維長Lは、以下の方法により算出した。まず、ガラス繊維強化樹脂板を、650℃のマッフル炉で0.5~24時間加熱して有機物を分解した。次いで、残存するガラス繊維をガラスシャーレに移し、アセトンを用いてガラス繊維をシャーレの表面に分散させた。次いで、シャーレ表面に分散したガラス繊維1000本以上について、実体顕微鏡を用いて繊維長を測定し、平均をとることで、ガラス繊維の数平均繊維長Lを算出した。表1~3中、ガラス繊維の数平均繊維長Lを「数平均繊維長L」と記載する。
ガラス繊維強化樹脂板における、ガラス繊維の数平均繊維長Lは、以下の方法により算出した。まず、ガラス繊維強化樹脂板を、650℃のマッフル炉で0.5~24時間加熱して有機物を分解した。次いで、残存するガラス繊維をガラスシャーレに移し、アセトンを用いてガラス繊維をシャーレの表面に分散させた。次いで、シャーレ表面に分散したガラス繊維1000本以上について、実体顕微鏡を用いて繊維長を測定し、平均をとることで、ガラス繊維の数平均繊維長Lを算出した。表1~3中、ガラス繊維の数平均繊維長Lを「数平均繊維長L」と記載する。
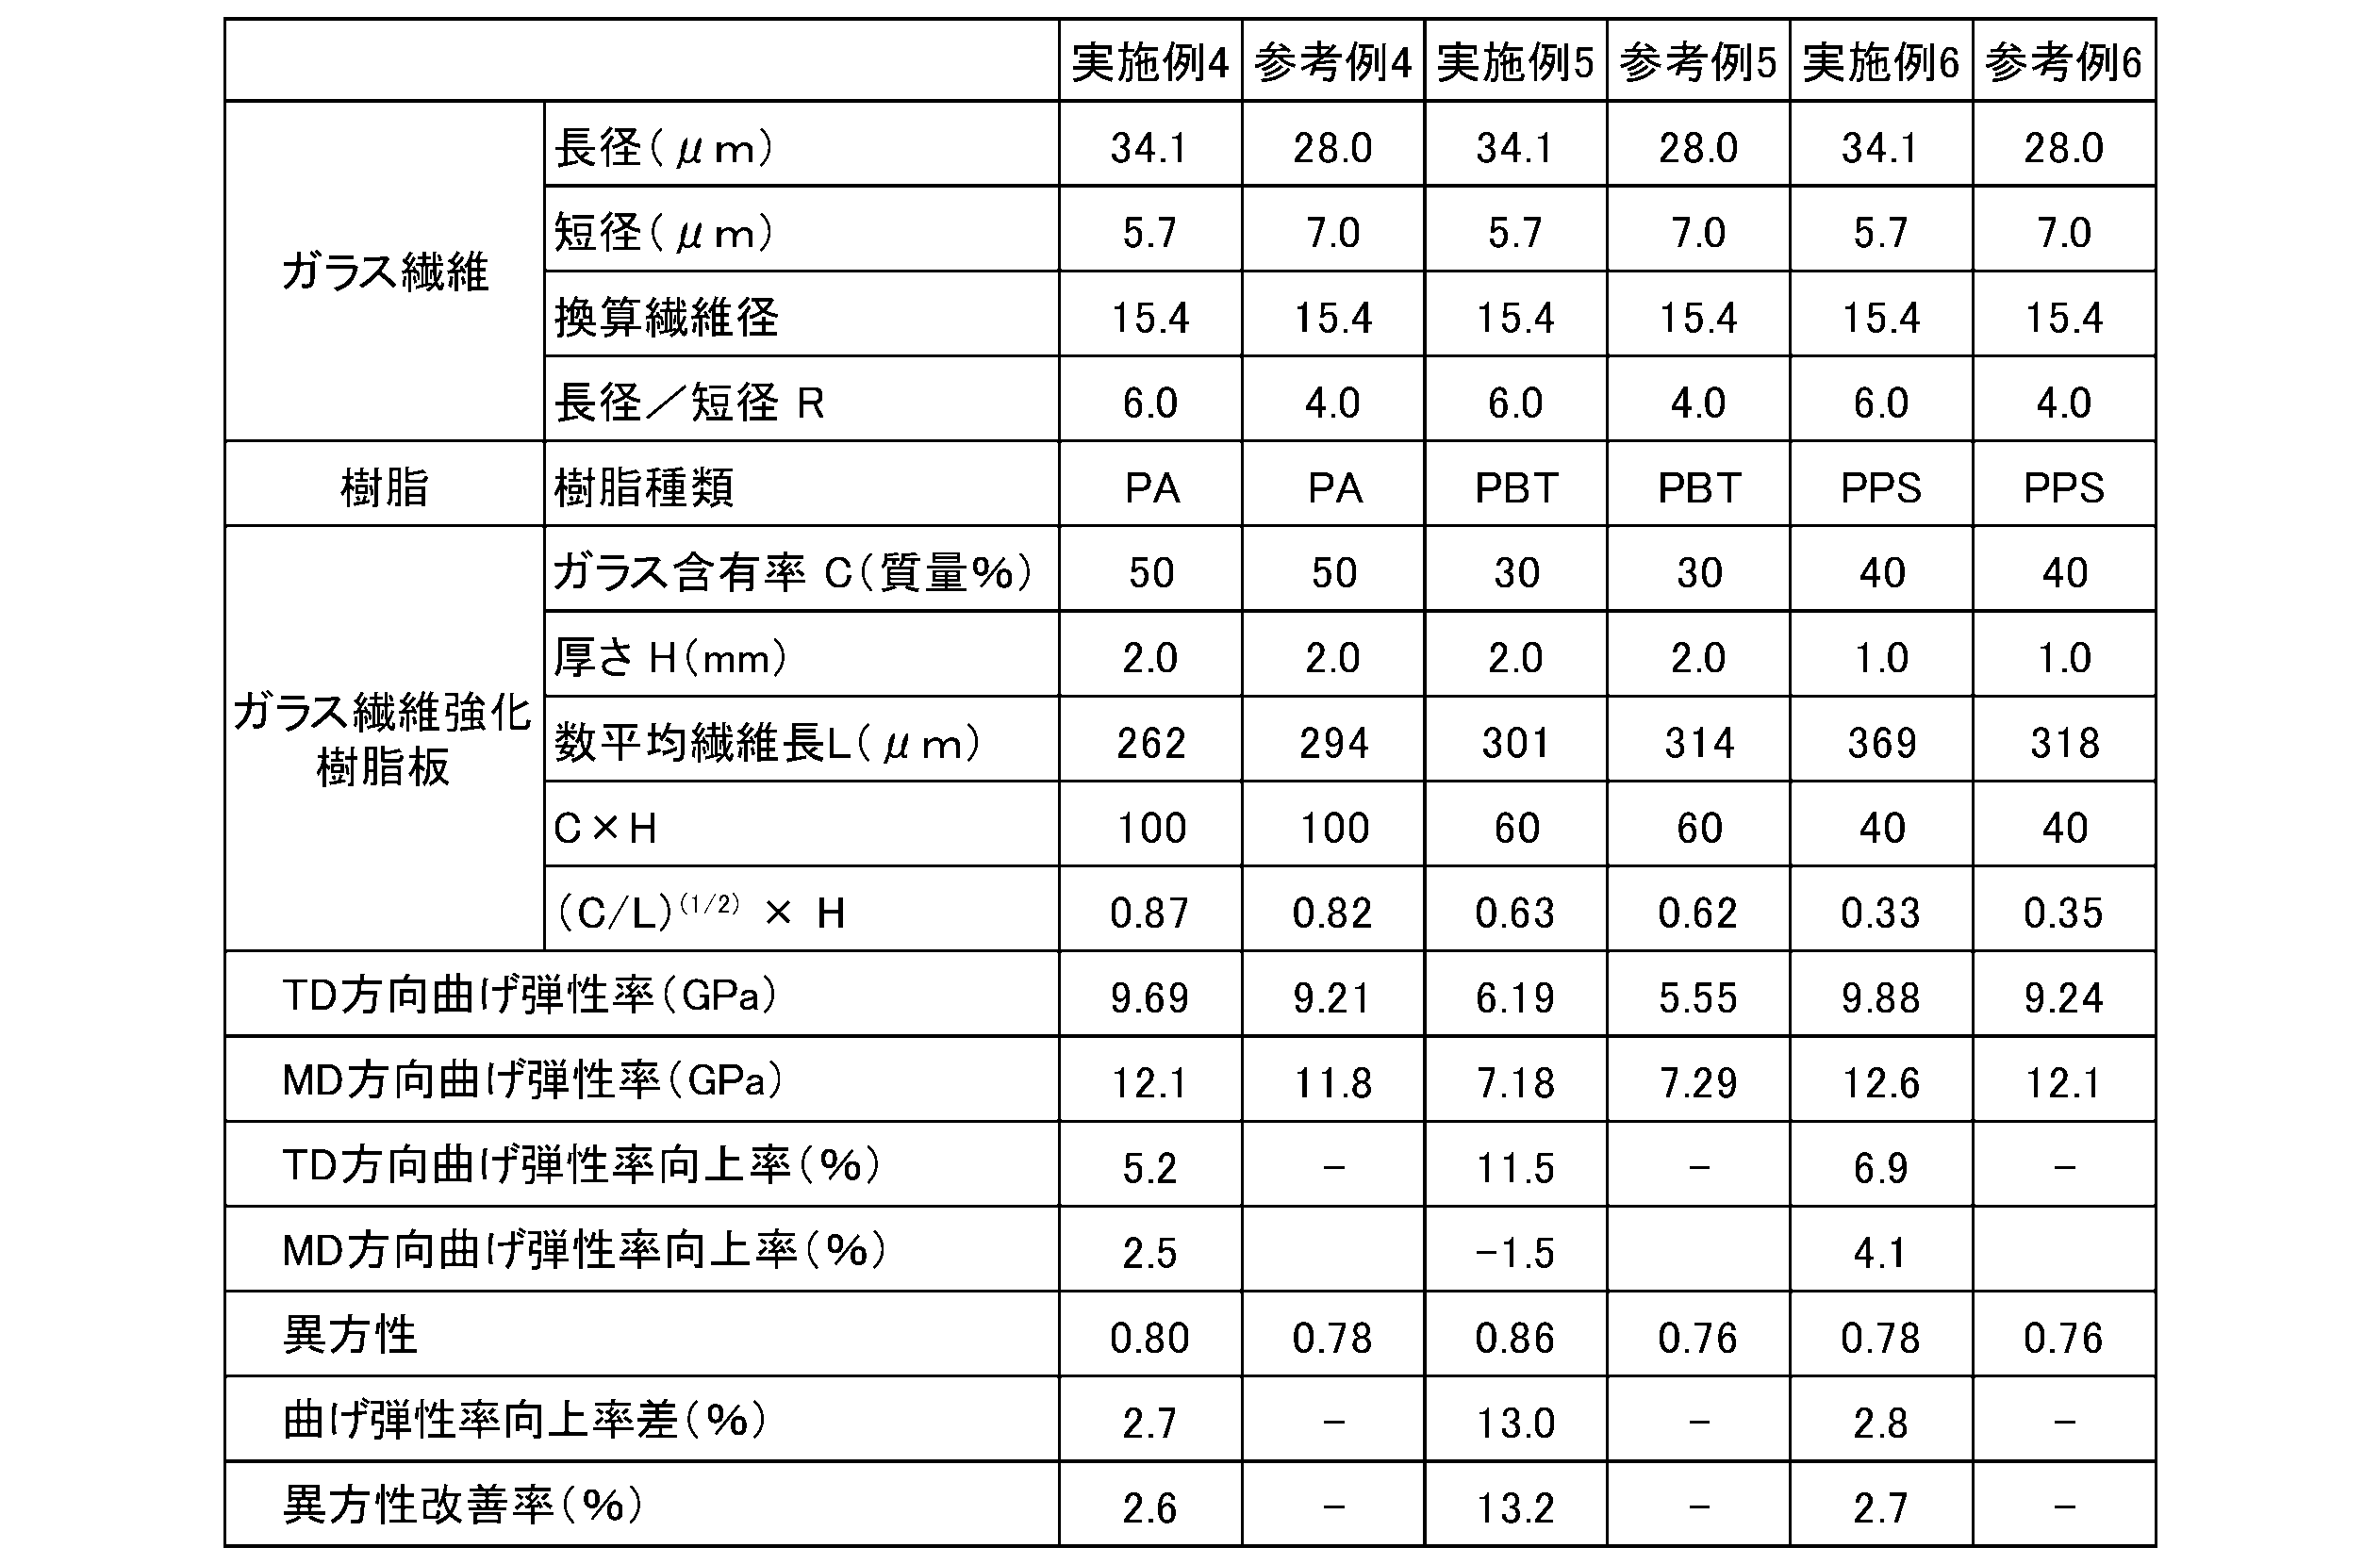
なお、表1~3において、TD方向曲げ弾性率向上率(%)、MD方向曲げ弾性率向上率(%)は、それぞれ対応する参考例のTD方向曲げ弾性率(GPa)、MD方向曲げ弾性率(GPa)に対する向上率であり、異方性改善率(%)は対応する参考例の異方性に対する改善率である。表1~3中、TD方向曲げ弾性率向上率とMD方向曲げ弾性率向上率との差(TD方向曲げ弾性率向上率-MD方向曲げ弾性率向上率)を「曲げ弾性率向上率差」と記載する。
〔参考例1〕
本参考例は、実施例1に対応する参考例であり、長径が28.0μm、短径が7.0μm、長径/短径Rが4.0、換算繊維径が15.4μmである長円形状の断面形状を備え、ガラスフィラメントが集束されてなるチョップドストランドを用いた以外は、実施例1と全く同一にして、ガラス含有率Cが40質量%の樹脂ペレットを作製した。
本参考例は、実施例1に対応する参考例であり、長径が28.0μm、短径が7.0μm、長径/短径Rが4.0、換算繊維径が15.4μmである長円形状の断面形状を備え、ガラスフィラメントが集束されてなるチョップドストランドを用いた以外は、実施例1と全く同一にして、ガラス含有率Cが40質量%の樹脂ペレットを作製した。
次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、ガラス繊維強化樹脂板(平板)を作成した。
次に、本参考例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表1に示す。
〔実施例2〕
本実施例では、ガラス含有率Cを50質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが1.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本実施例では、ガラス含有率Cを50質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが1.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本実施例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表1に示す。
〔参考例2〕
本参考例は、実施例2に対応する参考例であり、ガラス含有率Cを50質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが1.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本参考例は、実施例2に対応する参考例であり、ガラス含有率Cを50質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが1.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本参考例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表1に示す。
〔実施例3〕
本実施例では、ガラス含有率Cを30質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本実施例では、ガラス含有率Cを30質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本実施例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表1に示す。
〔参考例3〕
本参考例は、実施例3に対応する参考例であり、ガラス含有率Cを30質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本参考例は、実施例3に対応する参考例であり、ガラス含有率Cを30質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本参考例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表1に示す。
〔実施例4〕
本実施例では、ガラス含有率Cを50質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本実施例では、ガラス含有率Cを50質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本実施例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表2に示す。
〔参考例4〕
本参考例は、実施例4に対応する参考例であり、ガラス含有率Cを50質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本参考例は、実施例4に対応する参考例であり、ガラス含有率Cを50質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本参考例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表2に示す。
〔実施例5〕
本実施例では、ポリブチレンテレフタレート(ポリプラスチックス株式会社製、商品名:ジュラネックス2000、表2中、PBTと記載する)を用い、ガラス含有率Cを30質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用い、金型温度90℃、射出温度250℃とした以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本実施例では、ポリブチレンテレフタレート(ポリプラスチックス株式会社製、商品名:ジュラネックス2000、表2中、PBTと記載する)を用い、ガラス含有率Cを30質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用い、金型温度90℃、射出温度250℃とした以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本実施例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表2に示す。
〔参考例5〕
本参考例は、実施例5に対応する参考例であり、ポリブチレンテレフタレート(ポリプラスチックス株式会社製、商品名:ジュラネックス2000、表2中、PBTと記載する)を用い、ガラス含有率Cを30質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用い、金型温度90℃、射出温度250℃とした以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本参考例は、実施例5に対応する参考例であり、ポリブチレンテレフタレート(ポリプラスチックス株式会社製、商品名:ジュラネックス2000、表2中、PBTと記載する)を用い、ガラス含有率Cを30質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用い、金型温度90℃、射出温度250℃とした以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本参考例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表2に示す。
〔実施例6〕
本実施例では、ポリフェニレンスルフィド(クレハ株式会社製、商品名:フォートロンKPS W203A、表2中、PPSと記載する)を用い、ガラス含有率Cを40質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用い、金型温度140℃、射出温度310℃とした以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが1.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本実施例では、ポリフェニレンスルフィド(クレハ株式会社製、商品名:フォートロンKPS W203A、表2中、PPSと記載する)を用い、ガラス含有率Cを40質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本実施例で得られた樹脂ペレットを用い、金型温度140℃、射出温度310℃とした以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが1.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本実施例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表2に示す。
〔参考例6〕
本参考例は、実施例6に対応する参考例であり、ポリフェニレンスルフィド(クレハ株式会社製、商品名:フォートロンKPS W203A、表2中、PPSと記載する)を用い、ガラス含有率Cを40質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが1.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本参考例は、実施例6に対応する参考例であり、ポリフェニレンスルフィド(クレハ株式会社製、商品名:フォートロンKPS W203A、表2中、PPSと記載する)を用い、ガラス含有率Cを40質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが1.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本参考例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表2に示す。
〔比較例1〕
本比較例では、ガラス含有率Cを30質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本比較例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが0.8mmである、ガラス繊維強化樹脂板(平板)を作成した。
本比較例では、ガラス含有率Cを30質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本比較例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが0.8mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本比較例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表3に示す。
〔参考例7〕
本参考例は、比較例1に対応する参考例であり、ガラス含有率Cを30質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが0.8mmである、ガラス繊維強化樹脂板(平板)を作成した。
本参考例は、比較例1に対応する参考例であり、ガラス含有率Cを30質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが0.8mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本参考例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表3に示す。
〔比較例2〕
本比較例では、ガラス含有率Cを10質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本比較例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本比較例では、ガラス含有率Cを10質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本比較例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本比較例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表3に示す。
〔参考例8〕
本参考例は、比較例2に対応する参考例であり、ガラス含有率Cを10質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本参考例は、比較例2に対応する参考例であり、ガラス含有率Cを10質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本参考例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表3に示す。
〔比較例3〕
本比較例では、ガラス含有率Cを70質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本比較例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本比較例では、ガラス含有率Cを70質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本比較例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本比較例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表3に示す。
〔参考例9〕
本参考例は、比較例3に対応する参考例であり、ガラス含有率Cを70質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本参考例は、比較例3に対応する参考例であり、ガラス含有率Cを70質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用いた以外は、実施例1と全く同一にして、寸法が縦40mm×横25mmであり、厚さHが2.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本参考例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表3に示す。
〔比較例4〕
本比較例では、ポリカーボネート(帝人株式会社製、商品名:パンライトL-1250Y、表3中、PCと記載する)を用い、ガラス含有率Cを30質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本比較例で得られた樹脂ペレットを用い、金型温度110℃、射出温度290℃とした以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが0.8mmである、ガラス繊維強化樹脂板(平板)を作成した。
本比較例では、ポリカーボネート(帝人株式会社製、商品名:パンライトL-1250Y、表3中、PCと記載する)を用い、ガラス含有率Cを30質量%とした以外は、実施例1と全く同一にして、樹脂ペレットを作製した。次に、本比較例で得られた樹脂ペレットを用い、金型温度110℃、射出温度290℃とした以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが0.8mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本比較例で作成したガラス繊維強化樹脂板(平板)について、実施例1と全く同一にして、TD方向曲げ弾性率、及び、MD方向曲げ弾性率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。また、以下に述べる方法で全光線透過率を測定した。結果を表3に示す。
[全光線透過率]
ガラス繊維強化樹脂板を、幅30mm×長さ30mmに加工して、試験片を得た。次いで、得られた試験片について、分光光度計(株式会社日立ハイテクサイエンス製、商品名:分光光度計U-3900)を用いて、JIS K 7375:2008に準拠して、全光線透過率を測定した。
ガラス繊維強化樹脂板を、幅30mm×長さ30mmに加工して、試験片を得た。次いで、得られた試験片について、分光光度計(株式会社日立ハイテクサイエンス製、商品名:分光光度計U-3900)を用いて、JIS K 7375:2008に準拠して、全光線透過率を測定した。
〔参考例10〕
本参考例は、比較例4に対応する参考例であり、ポリカーボネートPC(帝人株式会社製、商品名:パンライトL-1250Y、表3中、PCと記載する)を用い、ガラス含有率Cを20質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用い、金型温度110℃、射出温度290℃とした以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが1.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
本参考例は、比較例4に対応する参考例であり、ポリカーボネートPC(帝人株式会社製、商品名:パンライトL-1250Y、表3中、PCと記載する)を用い、ガラス含有率Cを20質量%とした以外は、参考例1と全く同一にして、樹脂ペレットを作製した。次に、本参考例で得られた樹脂ペレットを用い、金型温度110℃、射出温度290℃とした以外は、実施例1と全く同一にして、寸法が縦20mm×横25mmであり、厚さHが1.0mmである、ガラス繊維強化樹脂板(平板)を作成した。
次に、本参考例で作成したガラス繊維強化樹脂板(平板)について、比較例4と全く同一にして、TD方向曲げ弾性率、MD方向曲げ弾性率、及び、全光線透過率を測定し、ガラス繊維強化樹脂板中のガラス繊維の数平均繊維長Lを算出した。結果を表3に示す。

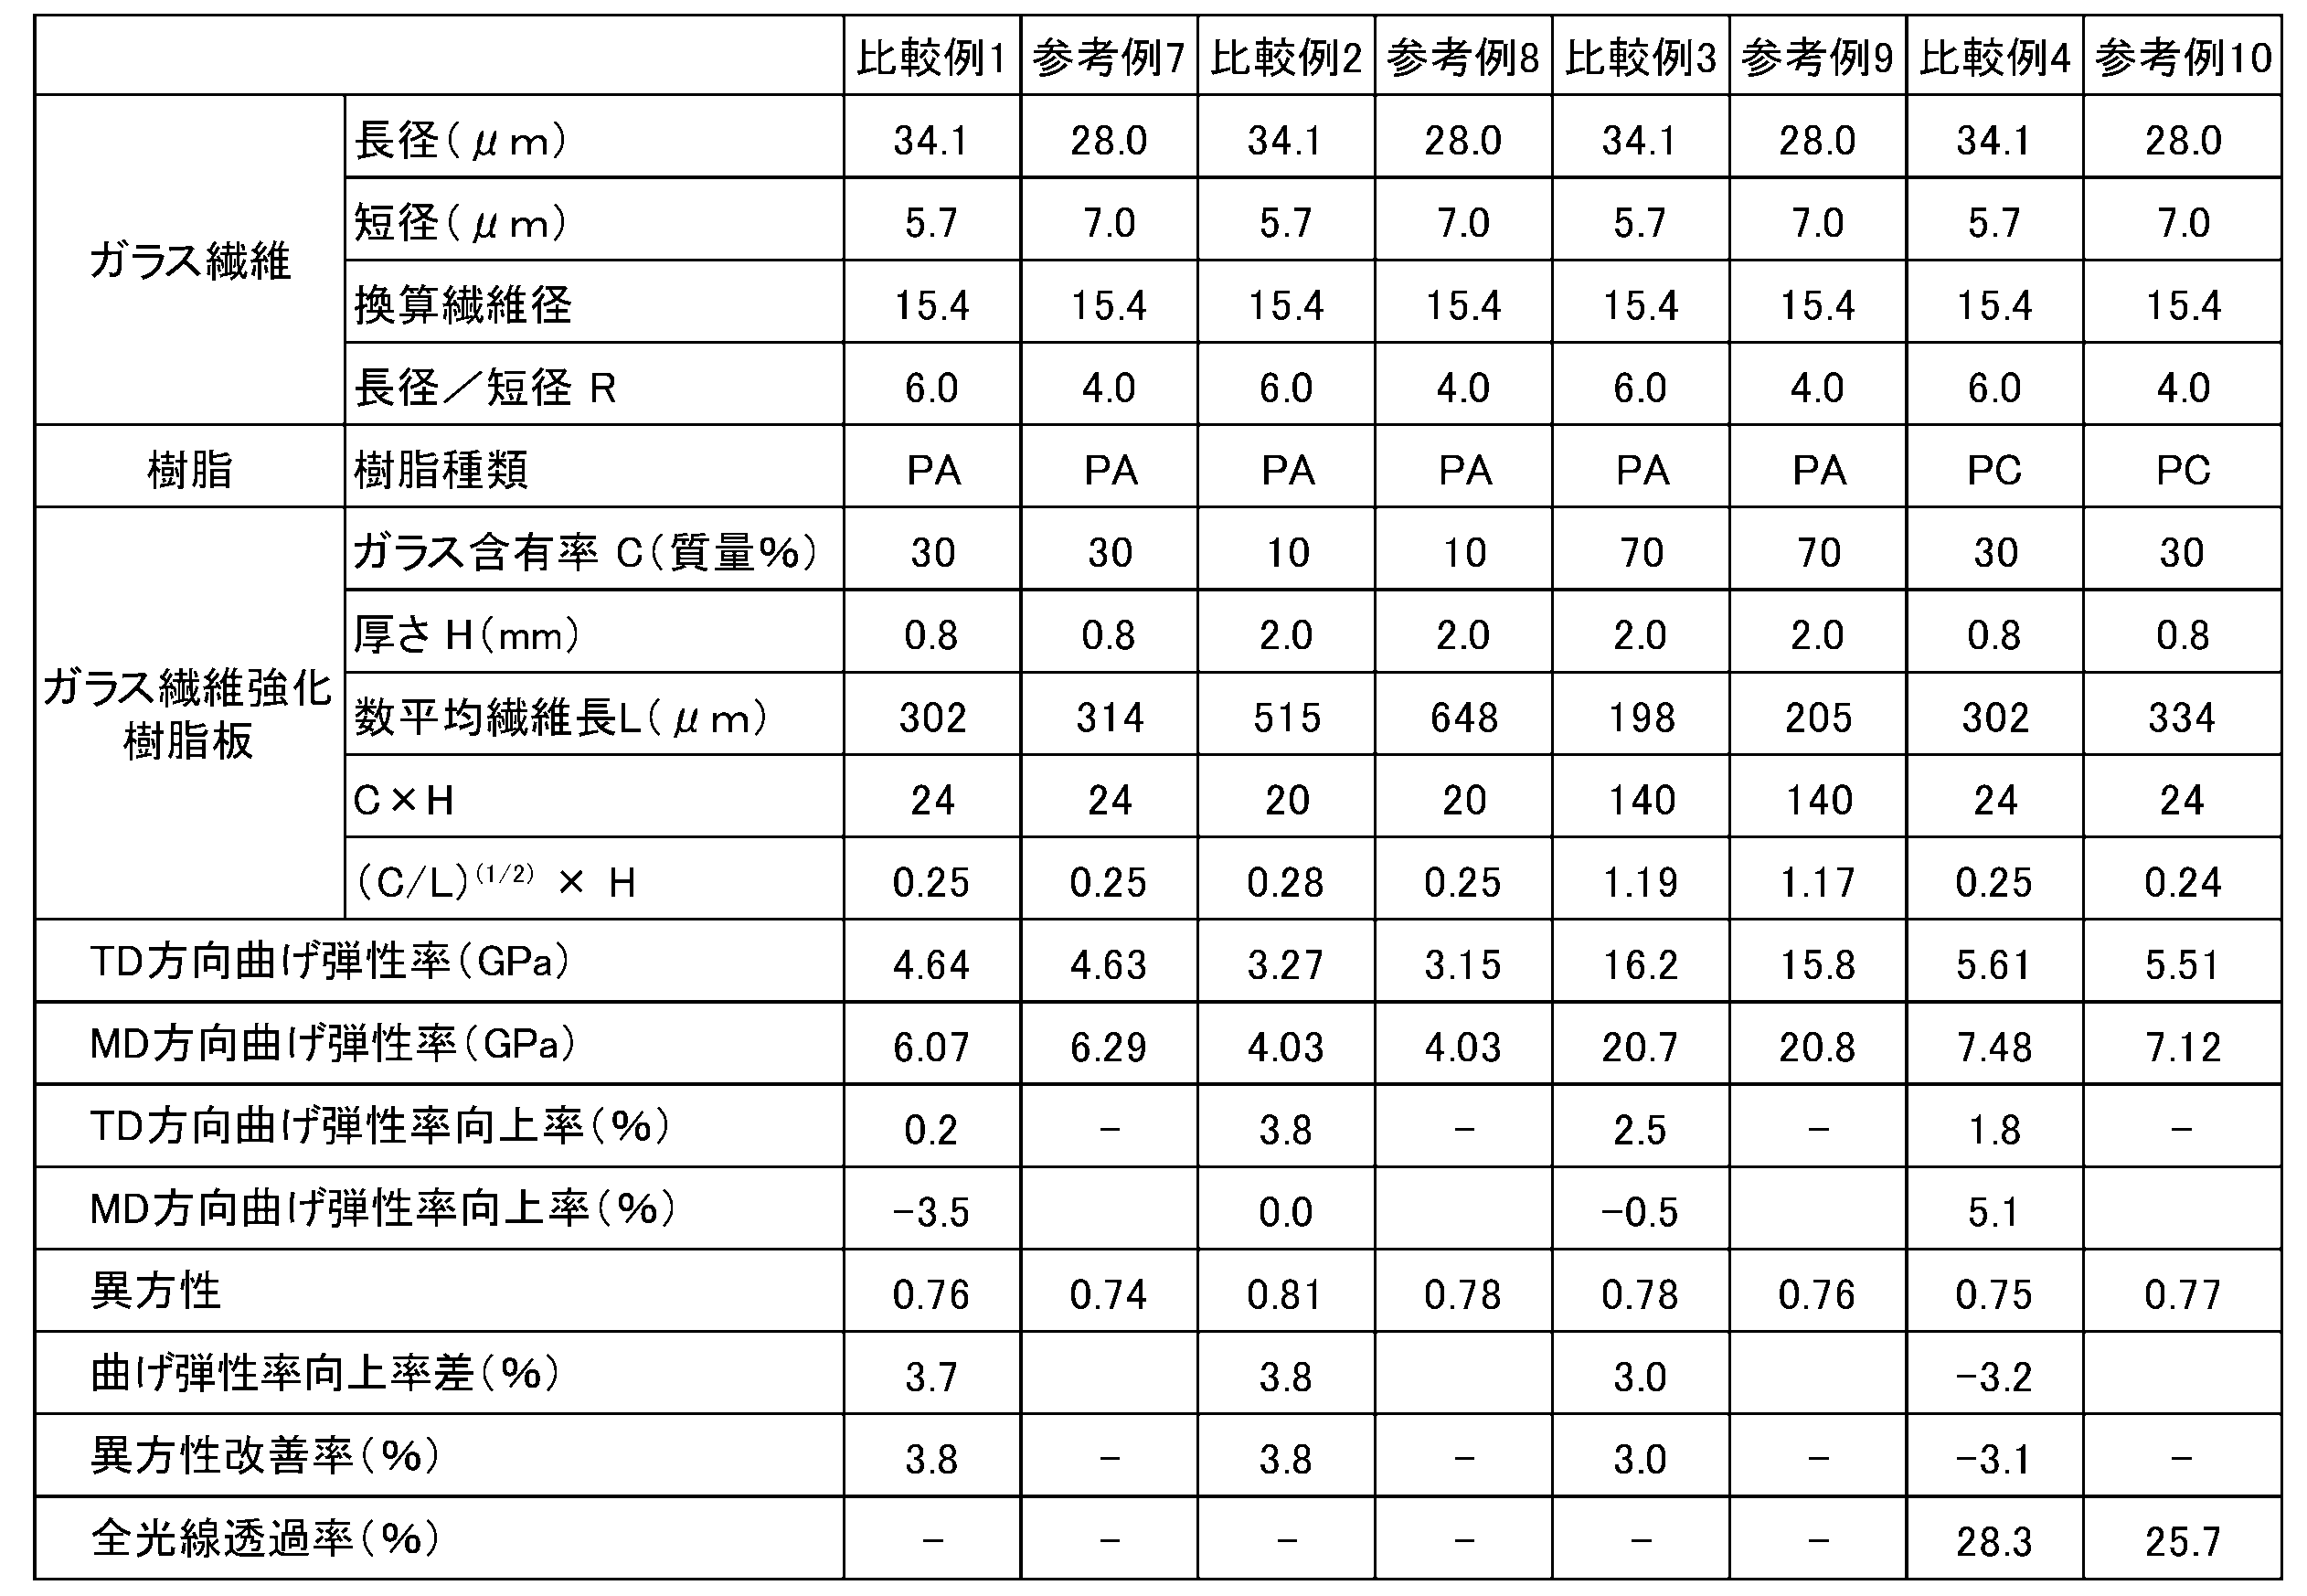
一方、表1~3から、ガラス繊維強化樹脂板におけるガラス繊維含有率C及び厚さHの積(H×C)が前記式(1)の範囲未満の比較例1、2、4のガラス繊維強化樹脂板、及び、ガラス繊維強化樹脂板におけるガラス繊維含有率C及び厚さHの積(H×C)が前記式(1)の範囲超の比較例3のガラス繊維強化樹脂板によれば、いずれもそれぞれ対応する参考例のTD方向曲げ弾性率(GPa)に対するTD方向曲げ弾性率向上率が、0.2~3.8%であり、実施例1~実施例6のガラス繊維強化樹脂板に比較して、TD方向の弾性率を向上することができないことが明らかである。
Claims (5)
- 扁平な断面形状を備えるガラス繊維と樹脂とを含むガラス繊維強化樹脂板であって、
前記扁平な断面形状を備えるガラス繊維は、短径が4.5~10.5μmの範囲にあり、長径が22.0~80.0μmの範囲にあり、前記短径に対する長径の比(長径/短径)Rが4.5~10.0の範囲にあり、
前記ガラス繊維強化樹脂板におけるガラス繊維含有率Cが、5.0~75.0質量%の範囲にあり、
前記ガラス繊維強化樹脂板の厚さHが0.5mm超10.0mm以下の範囲にあり、
前記C及びHが下記式(1)を満たすことを特徴とする、ガラス繊維強化樹脂板。
30.0≦H×C≦120.0 ・・・(1) - 請求項1記載のガラス繊維強化樹脂板において、前記ガラス繊維含有率Cが、20.0~60.0質量%の範囲にあり、前記ガラス繊維強化樹脂板の厚さHが、0.8~8.0mmの範囲にあり、前記C及びHが下記式(2)を満たすことを特徴とする、ガラス繊維強化樹脂板。
45.0≦H×C≦80.0 ・・・(2) - 請求項1又は請求項2記載のガラス繊維強化樹脂板において、前記ガラス繊維含有率Cが、20.0~40.0質量%の範囲にあり、前記ガラス繊維強化樹脂板の厚さHが、1.6~5.0mmの範囲にあり、前記C及びHが下記式(3)を満たすことを特徴とする、ガラス繊維強化樹脂板。
55.0≦H×C≦74.5 ・・・(3) - 請求項1~請求項3のいずれか1項記載のガラス繊維強化樹脂板において、前記ガラス繊維強化樹脂板に含まれる樹脂が、結晶性熱可塑性樹脂であることを特徴とする、ガラス繊維強化樹脂板。
- 請求項1~請求項4のいずれか1項記載のガラス繊維強化樹脂板において、前記ガラス繊維強化樹脂板に含まれる樹脂が、ポリアミドであることを特徴とする、ガラス繊維強化樹脂板。
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| KR1020227036593A KR20230066265A (ko) | 2020-09-11 | 2021-09-01 | 유리섬유 강화 수지판 |
| CN202180032712.XA CN115551952B (zh) | 2020-09-11 | 2021-09-01 | 玻璃纤维强化树脂板 |
| US17/917,974 US20230131534A1 (en) | 2020-09-11 | 2021-09-01 | Glass fiber-reinforced resin plate |
| JP2022547525A JP7636681B2 (ja) | 2020-09-11 | 2021-09-01 | ガラス繊維強化樹脂板 |
| EP21866619.6A EP4119610A4 (en) | 2020-09-11 | 2021-09-01 | GLASS FIBER REINFORCED RESIN BOARD |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2020-152951 | 2020-09-11 | ||
| JP2020152951 | 2020-09-11 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2022054660A1 true WO2022054660A1 (ja) | 2022-03-17 |
Family
ID=80631709
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2021/032095 Ceased WO2022054660A1 (ja) | 2020-09-11 | 2021-09-01 | ガラス繊維強化樹脂板 |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US20230131534A1 (ja) |
| EP (1) | EP4119610A4 (ja) |
| JP (1) | JP7636681B2 (ja) |
| KR (1) | KR20230066265A (ja) |
| CN (1) | CN115551952B (ja) |
| TW (1) | TWI910223B (ja) |
| WO (1) | WO2022054660A1 (ja) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP4095190A4 (en) * | 2020-10-15 | 2023-08-23 | Nitto Boseki Co., Ltd. | GLASS REINFORCED RESIN PANEL |
| CN119365335A (zh) * | 2022-06-22 | 2025-01-24 | 日东纺绩株式会社 | 金属-玻璃纤维强化热塑性树脂复合材料 |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2019081909A (ja) * | 2019-02-12 | 2019-05-30 | 日東紡績株式会社 | ガラス繊維強化樹脂成形品 |
| CN118715186B (zh) * | 2023-01-26 | 2025-04-01 | 日东纺绩株式会社 | 扁平截面玻璃纤维、玻璃纤维强化树脂组合物以及玻璃纤维强化树脂成型品 |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2002105333A (ja) * | 2000-06-28 | 2002-04-10 | Matsushita Electric Works Ltd | 熱可塑性樹脂組成物、その製造方法、並びに半導体素子収納用パッケージ |
| JP2003268224A (ja) * | 2002-03-20 | 2003-09-25 | Mitsubishi Engineering Plastics Corp | 精密成形部品 |
| JP2010084007A (ja) | 2008-09-30 | 2010-04-15 | Mitsubishi Engineering Plastics Corp | 携帯電子機器用ポリアミド樹脂組成物及び携帯電子機器部品 |
| JP2011016902A (ja) * | 2009-07-08 | 2011-01-27 | Teijin Chem Ltd | 導電性樹脂組成物からなる成形品 |
| WO2015029780A1 (ja) * | 2013-08-30 | 2015-03-05 | 東洋紡株式会社 | 吸水時の振動性と外観に優れた高融点ポリアミド樹脂組成物 |
| WO2017131018A1 (ja) * | 2016-01-29 | 2017-08-03 | 株式会社クラレ | 成形品及びその製造方法 |
| WO2018182038A1 (ja) | 2017-03-31 | 2018-10-04 | 新日鉄住金化学株式会社 | 金属-繊維強化樹脂材料複合体及びその製造方法 |
| JP2019094466A (ja) * | 2017-11-27 | 2019-06-20 | 住友化学株式会社 | 液晶ポリエステル樹脂組成物および成形体 |
| JP2019209509A (ja) * | 2018-05-31 | 2019-12-12 | 日本電気硝子株式会社 | 繊維強化樹脂 |
| WO2020137004A1 (ja) * | 2018-12-27 | 2020-07-02 | 日東紡績株式会社 | ガラス繊維強化樹脂成形品 |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2007080754A1 (ja) * | 2006-01-13 | 2007-07-19 | Mitsubishi Engineering-Plastics Corporation | 携帯電子機器用ポリアミド樹脂組成物および携帯電子機器用成形品 |
| US7858172B2 (en) * | 2006-05-25 | 2010-12-28 | Mitsubishi Engineering-Plastics Corporation | Fiber-reinforced thermoplastic resin molded article |
| JP5275689B2 (ja) * | 2008-06-05 | 2013-08-28 | 出光興産株式会社 | 繊維強化ポリカーボネート系樹脂組成物及びその成形体 |
| JP2010105226A (ja) * | 2008-10-29 | 2010-05-13 | Teijin Chem Ltd | 樹脂成形体 |
| JP2010222486A (ja) * | 2009-03-24 | 2010-10-07 | Unitika Ltd | 難燃性ガラス繊維強化ポリアミド樹脂組成物 |
| JP2013103981A (ja) * | 2011-11-14 | 2013-05-30 | Nippon Electric Glass Co Ltd | ガラス繊維、及びガラス繊維強化ポリカーボネート樹脂 |
| CN104144983A (zh) * | 2012-02-23 | 2014-11-12 | 东丽株式会社 | 热塑性树脂组合物和成型品 |
| JP6790812B2 (ja) * | 2016-12-26 | 2020-11-25 | 日東紡績株式会社 | ガラス繊維強化樹脂成形品 |
| JP6912922B2 (ja) | 2017-04-12 | 2021-08-04 | ソニーセミコンダクタソリューションズ株式会社 | 固体撮像素子 |
| WO2020004597A1 (ja) * | 2018-06-29 | 2020-01-02 | 出光興産株式会社 | 樹脂金属複合体及びその製造方法 |
-
2021
- 2021-09-01 CN CN202180032712.XA patent/CN115551952B/zh active Active
- 2021-09-01 WO PCT/JP2021/032095 patent/WO2022054660A1/ja not_active Ceased
- 2021-09-01 KR KR1020227036593A patent/KR20230066265A/ko active Pending
- 2021-09-01 EP EP21866619.6A patent/EP4119610A4/en active Pending
- 2021-09-01 TW TW110132396A patent/TWI910223B/zh active
- 2021-09-01 US US17/917,974 patent/US20230131534A1/en active Pending
- 2021-09-01 JP JP2022547525A patent/JP7636681B2/ja active Active
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2002105333A (ja) * | 2000-06-28 | 2002-04-10 | Matsushita Electric Works Ltd | 熱可塑性樹脂組成物、その製造方法、並びに半導体素子収納用パッケージ |
| JP2003268224A (ja) * | 2002-03-20 | 2003-09-25 | Mitsubishi Engineering Plastics Corp | 精密成形部品 |
| JP2010084007A (ja) | 2008-09-30 | 2010-04-15 | Mitsubishi Engineering Plastics Corp | 携帯電子機器用ポリアミド樹脂組成物及び携帯電子機器部品 |
| JP2011016902A (ja) * | 2009-07-08 | 2011-01-27 | Teijin Chem Ltd | 導電性樹脂組成物からなる成形品 |
| WO2015029780A1 (ja) * | 2013-08-30 | 2015-03-05 | 東洋紡株式会社 | 吸水時の振動性と外観に優れた高融点ポリアミド樹脂組成物 |
| WO2017131018A1 (ja) * | 2016-01-29 | 2017-08-03 | 株式会社クラレ | 成形品及びその製造方法 |
| WO2018182038A1 (ja) | 2017-03-31 | 2018-10-04 | 新日鉄住金化学株式会社 | 金属-繊維強化樹脂材料複合体及びその製造方法 |
| JP2019094466A (ja) * | 2017-11-27 | 2019-06-20 | 住友化学株式会社 | 液晶ポリエステル樹脂組成物および成形体 |
| JP2019209509A (ja) * | 2018-05-31 | 2019-12-12 | 日本電気硝子株式会社 | 繊維強化樹脂 |
| WO2020137004A1 (ja) * | 2018-12-27 | 2020-07-02 | 日東紡績株式会社 | ガラス繊維強化樹脂成形品 |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP4119610A4 |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP4095190A4 (en) * | 2020-10-15 | 2023-08-23 | Nitto Boseki Co., Ltd. | GLASS REINFORCED RESIN PANEL |
| CN119365335A (zh) * | 2022-06-22 | 2025-01-24 | 日东纺绩株式会社 | 金属-玻璃纤维强化热塑性树脂复合材料 |
Also Published As
| Publication number | Publication date |
|---|---|
| JP7636681B2 (ja) | 2025-02-27 |
| KR20230066265A (ko) | 2023-05-15 |
| EP4119610A1 (en) | 2023-01-18 |
| JPWO2022054660A1 (ja) | 2022-03-17 |
| CN115551952A (zh) | 2022-12-30 |
| US20230131534A1 (en) | 2023-04-27 |
| CN115551952B (zh) | 2023-12-08 |
| TW202222928A (zh) | 2022-06-16 |
| TWI910223B (zh) | 2026-01-01 |
| EP4119610A4 (en) | 2024-04-10 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP7410411B2 (ja) | ガラス繊維強化樹脂成形品 | |
| EP3795642B1 (en) | Glass fiber-reinforced resin molded article | |
| KR102403724B1 (ko) | 유리 섬유 강화 수지 성형품 | |
| JP7636681B2 (ja) | ガラス繊維強化樹脂板 | |
| JP7070819B1 (ja) | ガラス繊維強化樹脂成形品 | |
| JP6901055B1 (ja) | ガラスダイレクトロービング、及び、ガラス長繊維強化熱可塑性樹脂ペレット | |
| WO2021157162A1 (ja) | ガラス繊維強化樹脂組成物及びガラス繊維強化樹脂成形品 | |
| JP2021091907A (ja) | ガラス繊維強化樹脂成形品 | |
| JP7063424B1 (ja) | ガラス繊維強化樹脂板 | |
| JP7856911B2 (ja) | ガラス強化樹脂成形品 | |
| WO2021199497A1 (ja) | ガラスダイレクトロービング、及び、ガラス長繊維強化熱可塑性樹脂ペレット | |
| US12195600B1 (en) | Flat-cross-section glass fiber, glass-fiber-reinforced resin composition, and glass-fiber-reinforced resin molded product | |
| JP7393714B1 (ja) | 扁平断面ガラス繊維、ガラス繊維強化樹脂組成物およびガラス繊維強化樹脂成形品 | |
| WO2023248493A1 (ja) | 金属-ガラス繊維強化熱可塑性樹脂複合材料 | |
| WO2022138382A1 (ja) | 金属-ガラス繊維強化熱可塑性樹脂複合材料 | |
| WO2024038547A1 (ja) | 扁平断面ガラス繊維、及び、ガラス再生材料を含むガラス原料からの扁平断面ガラス繊維の製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 21866619 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2022547525 Country of ref document: JP Kind code of ref document: A |
|
| ENP | Entry into the national phase |
Ref document number: 2021866619 Country of ref document: EP Effective date: 20221010 |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |