WO2023106002A1 - 被膜付きフィルムからの被膜の剥離方法および被膜の剥離装置 - Google Patents
被膜付きフィルムからの被膜の剥離方法および被膜の剥離装置 Download PDFInfo
- Publication number
- WO2023106002A1 WO2023106002A1 PCT/JP2022/040912 JP2022040912W WO2023106002A1 WO 2023106002 A1 WO2023106002 A1 WO 2023106002A1 JP 2022040912 W JP2022040912 W JP 2022040912W WO 2023106002 A1 WO2023106002 A1 WO 2023106002A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- coating
- film
- coated film
- peeling
- coated
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images







Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D—PROCESSES FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05D3/00—Pretreatment of surfaces to which liquids or other fluent materials are to be applied; After-treatment of applied coatings, e.g. intermediate treating of an applied coating preparatory to subsequent applications of liquids or other fluent materials
- B05D3/10—Pretreatment of surfaces to which liquids or other fluent materials are to be applied; After-treatment of applied coatings, e.g. intermediate treating of an applied coating preparatory to subsequent applications of liquids or other fluent materials by other chemical means
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08J—WORKING-UP; GENERAL PROCESSES OF COMPOUNDING; AFTER-TREATMENT NOT COVERED BY SUBCLASSES C08B, C08C, C08F, C08G or C08H
- C08J11/00—Recovery or working-up of waste materials
- C08J11/04—Recovery or working-up of waste materials of polymers
- C08J11/06—Recovery or working-up of waste materials of polymers without chemical reactions
- C08J11/08—Recovery or working-up of waste materials of polymers without chemical reactions using selective solvents for polymer components
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B08—CLEANING
- B08B—CLEANING IN GENERAL; PREVENTION OF FOULING IN GENERAL
- B08B1/00—Cleaning by methods involving the use of tools
- B08B1/20—Cleaning of moving articles, e.g. of moving webs or of objects on a conveyor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B08—CLEANING
- B08B—CLEANING IN GENERAL; PREVENTION OF FOULING IN GENERAL
- B08B3/00—Cleaning by methods involving the use or presence of liquid or steam
- B08B3/02—Cleaning by the force of jets or sprays
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B08—CLEANING
- B08B—CLEANING IN GENERAL; PREVENTION OF FOULING IN GENERAL
- B08B3/00—Cleaning by methods involving the use or presence of liquid or steam
- B08B3/04—Cleaning involving contact with liquid
- B08B3/041—Cleaning travelling work
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29B—PREPARATION OR PRETREATMENT OF THE MATERIAL TO BE SHAPED; MAKING GRANULES OR PREFORMS; RECOVERY OF PLASTICS OR OTHER CONSTITUENTS OF WASTE MATERIAL CONTAINING PLASTICS
- B29B17/00—Recovery of plastics or other constituents of waste material containing plastics
- B29B17/02—Separating plastics from other materials
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B32—LAYERED PRODUCTS
- B32B—LAYERED PRODUCTS, i.e. PRODUCTS BUILT-UP OF STRATA OF FLAT OR NON-FLAT, e.g. CELLULAR OR HONEYCOMB, FORM
- B32B7/00—Layered products characterised by the relation between layers; Layered products characterised by the relative orientation of features between layers, or by the relative values of a measurable parameter between layers, i.e. products comprising layers having different physical, chemical or physicochemical properties; Layered products characterised by the interconnection of layers
- B32B7/04—Interconnection of layers
- B32B7/06—Interconnection of layers permitting easy separation
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29B—PREPARATION OR PRETREATMENT OF THE MATERIAL TO BE SHAPED; MAKING GRANULES OR PREFORMS; RECOVERY OF PLASTICS OR OTHER CONSTITUENTS OF WASTE MATERIAL CONTAINING PLASTICS
- B29B17/00—Recovery of plastics or other constituents of waste material containing plastics
- B29B17/02—Separating plastics from other materials
- B29B2017/0213—Specific separating techniques
- B29B2017/0217—Mechanical separating techniques; devices therefor
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29B—PREPARATION OR PRETREATMENT OF THE MATERIAL TO BE SHAPED; MAKING GRANULES OR PREFORMS; RECOVERY OF PLASTICS OR OTHER CONSTITUENTS OF WASTE MATERIAL CONTAINING PLASTICS
- B29B17/00—Recovery of plastics or other constituents of waste material containing plastics
- B29B17/02—Separating plastics from other materials
- B29B2017/0213—Specific separating techniques
- B29B2017/0286—Cleaning means used for separation
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29B—PREPARATION OR PRETREATMENT OF THE MATERIAL TO BE SHAPED; MAKING GRANULES OR PREFORMS; RECOVERY OF PLASTICS OR OTHER CONSTITUENTS OF WASTE MATERIAL CONTAINING PLASTICS
- B29B17/00—Recovery of plastics or other constituents of waste material containing plastics
- B29B17/02—Separating plastics from other materials
- B29B2017/0213—Specific separating techniques
- B29B2017/0293—Dissolving the materials in gases or liquids
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B29—WORKING OF PLASTICS; WORKING OF SUBSTANCES IN A PLASTIC STATE IN GENERAL
- B29L—INDEXING SCHEME ASSOCIATED WITH SUBCLASS B29C, RELATING TO PARTICULAR ARTICLES
- B29L2009/00—Layered products
- B29L2009/005—Layered products coated
-
- C—CHEMISTRY; METALLURGY
- C08—ORGANIC MACROMOLECULAR COMPOUNDS; THEIR PREPARATION OR CHEMICAL WORKING-UP; COMPOSITIONS BASED THEREON
- C08J—WORKING-UP; GENERAL PROCESSES OF COMPOUNDING; AFTER-TREATMENT NOT COVERED BY SUBCLASSES C08B, C08C, C08F, C08G or C08H
- C08J2383/00—Characterised by the use of macromolecular compounds obtained by reactions forming in the main chain of the macromolecule a linkage containing silicon with or without sulfur, nitrogen, oxygen, or carbon only; Derivatives of such polymers
- C08J2383/04—Polysiloxanes
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02W—CLIMATE CHANGE MITIGATION TECHNOLOGIES RELATED TO WASTEWATER TREATMENT OR WASTE MANAGEMENT
- Y02W30/00—Technologies for solid waste management
- Y02W30/50—Reuse, recycling or recovery technologies
- Y02W30/62—Plastics recycling; Rubber recycling
Definitions
- the present invention relates to a film peeling method and a film peeling apparatus capable of efficiently removing a film on the surface of a thermoplastic resin film.
- a general method for manufacturing this MLCC includes steps of using a release film obtained by forming a release layer on a plastic base film as a carrier sheet, forming a ceramic green sheet layer on the release film, and There is a step of peeling off the ceramic green sheet layer to form a ceramic green sheet.
- the release film from which the ceramic green sheet layer has been peeled off is discarded as an unnecessary material. That is, the recent rapid increase in the number of MLCCs has led to an increase in the amount of release film waste, which has become an environmental problem, and efforts have been made to recycle plastic substrate films. In order to reuse the discarded release film, it is possible to obtain a recycled film by recovering/crushing/making into resin chips and then remelting and forming a film.
- the components of the release layer contained in the release film generally have a different composition from the components that make up the base film. is pulverized into resin chips and then melted again to form a film, since the components of the release layer are present as foreign matter, stable film formation becomes difficult.
- Patent Document 1 as a method for removing a release component from a release film, a release film in which a water-soluble resin layer is formed between a base film and a release layer is used, and is placed in a hot liquid bath for 2 seconds. A method for peeling off the release layer by rubbing the surface of the release film with a brush roll after the above immersion is disclosed.
- the present invention provides a film with a coating that can be peeled off at high speed by dissolving a water-soluble resin in a short time using a cleaning solution after scratching the surface of the film with a coating after use.
- a coating stripping method and coating stripping apparatus are provided.
- a method for peeling a coating of the present invention for solving the above problems is a method for peeling a coating from a coated film having a coating on at least one side of a base film, the surface of the coated film having the coating scratching, scoring, or forming a hole in the coating from, or scratching, scoring, or forming a hole reaching the coating from the non-coated side of the coated film, and then The cleaning solution is brought into contact with the coating, and then the coating containing the cleaning solution is peeled off from the coated film.
- the scratches are made so that the angle (acute angle) formed by the longitudinal direction of the scratches and the transport direction is 60 degrees or less.
- the film preferably contains a water-soluble resin.
- the coating preferably contains a curable silicone resin.
- the washing liquid is preferably water.
- the coating peeling device of the present invention for solving the above problems is a coating peeling device from a coated film having a coating on at least one side of a base film, wherein the coating surface of the coated film a coating damage mechanism that scratches, slits, or forms holes in the coating from, or scratches, slits, or holes that reach the coating from the non-coated side of the coated film , a cleaning liquid application mechanism for applying a cleaning liquid to the coating of the coated film having the scratch, the notch, or the hole; a peeling mechanism for peeling the coating containing the cleaning liquid from the coated film; It has [7]
- the coating peeling device of [6] above includes a transport mechanism that transports the film with the coating, and the coating damage mechanism causes the scratch to form an angle (acute angle) between the longitudinal direction of the scratch and the transport direction.
- the coating peeling device of [6] or [7] includes an unwinding device for unwinding the coated film wound in a roll and the base film from which the coating has been peeled off. and a winding device for winding.
- the water-soluble resin can be dissolved from the surface of the coated film using a cleaning liquid in a short time, and the coating can be peeled off at high speed. can be done with
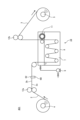
- FIG. 1 is a schematic diagram of a peeling device 101 according to a first embodiment of the invention; FIG. It is the schematic of the peeling apparatus 201 of the 2nd Embodiment of this invention. It is the schematic of the peeling apparatus 301 of the 3rd Embodiment of this invention.
- Figure 4 is a schematic top view of the coating damage mechanism 6 of Figure 3; It is the schematic of the peeling apparatus 401 of the 4th Embodiment of this invention.
- 6 is a schematic top view of the coating damage mechanism 6 of FIG. 5;
- FIG. 10 is a schematic top view of the coating damage mechanism 6 of FIG. 9; It is a schematic diagram of a peeling device 801 of an eighth embodiment of the present invention. 12 is a schematic top view of the coating damage mechanism 6 of FIG. 11; FIG. It is a schematic diagram of a peeling device 901 of a ninth embodiment of the present invention. 14 is a schematic top view of the coating damage mechanism 6 of FIG. 13; FIG. It is the schematic of the peeling apparatus 111 of the 10th Embodiment of this invention. 16 is a schematic top view of the coating damage mechanism 6 of FIG. 15; FIG.
- the inventors of the present invention have made intensive studies on a method of dissolving the coating resin in a short time using a cleaning agent to enable the coating to be peeled off at high speed. I found the device.
- the coating stripping method of the coated film of the present invention is a method for cleaning a coated film having a coating on the surface of a base film and peeling and removing the coating from the base film.
- the coating may be on one side or both sides of the base film, and is not particularly limited.
- the target coating of the coated film can be a coating of any composition, but a coating containing a water-soluble resin is preferable in consideration of the load on the environment.
- At least one of water-soluble polyester-based resin, polyester-urethane-based resin, acrylic-based resin, ethylene ionomer-based resin, polyvinyl alcohol-based resin, polyvinylpyrrolidone-based resin, ethylene-vinyl alcohol-based resin, and starch as the water-soluble resin. is more preferable as a main component.
- the film containing the water-soluble resin may be a single layer containing the water-soluble resin or a laminate of two or more layers containing the water-soluble resin. It may be a laminate of layers that do not contain.
- a coated release film containing a part of the coating in addition to the water-soluble resin as well as a release component is particularly preferable, and the effect of peeling the coating can be efficiently exhibited.
- the term "releasing component" as used herein refers to a component that increases the contact angle of the film surface with water, that is, reduces the surface energy of the film.
- the release component is, for example, a thermosetting silicone resin compound having a dimethylsiloxane as a main skeleton, or an organopolysiloxane containing an acryloyl group or a methacryloyl group, which is blended with a photopolymerization initiator and cured by irradiation with UV light.
- curable silicone resins such as UV curable silicone resin compounds that are cured, compounds having long-chain alkyl groups, and compounds having fluorine.
- the film may be a mixture of a water-soluble resin and a release component, or may be a laminate of a layer containing a water-soluble resin and a layer containing a release component.
- a layer containing a water-soluble resin is formed immediately above the base film, and then a layer containing a release component is formed on the outermost surface.
- the method of peeling the coating from the coated film of the present invention involves scratching, cutting, or forming holes in the coating from the coated surface of the coated film, or A scratch, cut, or hole is made to reach the coating from the non-coating surface of the coated film, then the cleaning solution is brought into contact with the coating, and then the coating containing the cleaning solution is peeled off from the coated film. That is, it is characterized by damaging the coating by scratching, cutting, or forming holes in the coating before contacting the cleaning solution with the coating, allowing the cleaning solution to penetrate efficiently into the coating, and cleaning the coating for a short period of time. to dissolve the film.
- “scratch” means to roughen the coating surface to form unevenness by physically rubbing the coating
- “cut” means to bring a sharp object into contact with the coating. In other words, it means to make a cut in the coating
- "form a hole” means to form a round hole, a polygonal hole, or the like in the coating.
- the dissolution of the water-soluble resin proceeds as the cleaning liquid permeates from the film surface.
- the contact area with the cleaning solution increases, and the coating has unevenness, cuts, and holes, which make it easier for the cleaning solution to spread to deeper positions in the thickness direction of the coating.
- soluble resin In the case where the coating of the target coated film is a layer containing a water-soluble resin immediately above the base film, and then a laminated coating containing a release component on the outermost surface, scratches penetrating the outermost layer By forming a groove, a notch, or a hole, the cleaning liquid can be efficiently guided to the underlying layer containing the water-soluble resin.
- the contact area with the cleaning liquid increases, and the layer containing the water-soluble resin has no unevenness, cuts, or holes. Since the cleaning liquid can easily spread to a deeper position in the thickness direction of the film, the water-soluble resin can be dissolved in a short time.
- the scratches, cuts, and holes may reach the base film, and in this case, the contact area with the cleaning liquid can be further increased in the thickness direction of the layer containing the water-soluble resin.
- thermosetting silicone resin compound having a main skeleton of dimethyl chloroxane which has high permeability to the cleaning liquid
- the cleaning liquid Permeates through the surface of the film and easily reaches the layer containing the water-soluble resin.
- the formation of scratches, cuts, and holes promotes penetration, so it dissolves the water-soluble resin in the lower layer in a short time. be able to.
- a scratch, cut, or hole may be formed from the non-coating surface to reach the coating.
- a force acts in the direction in which the layer containing the water-soluble resin is extruded from the base film, so that it is possible to avoid being buried in the base film.
- the washing liquid can be expected to permeate from the coating surface side and from the rear surface of the base film through scratches, cuts, and holes on the base film side, so that the dissolution of the water-soluble resin can be further promoted.
- the coated film when scratching, it is preferable to scratch the coated film while conveying it so that the angle (acute angle) formed by the longitudinal direction of the scratch and the conveying direction is 60° or less.
- the cut when the cut is made, it is preferable to make the cut so that the angle (acute angle) formed by the longitudinal direction of the cut and the conveying direction is 60° or less.
- a scratch or cut is made to reach a part of the base film, the conveying tension of the film is large, and the angle between the longitudinal direction of the scratch or cut and the conveying direction is 90 °. may act perpendicularly to scratches and cuts, leading to elongation and breakage of the base film.
- the angle between the longitudinal direction of the scratches or cuts and the conveying direction is preferably 60° or less, which makes it difficult for the film to stretch or break.
- the temperature of the cleaning liquid is preferably 150° C. or lower in order to suppress the dimensional change of the base film due to heat. Therefore, it is preferable that the temperature of the cleaning liquid is adjusted according to the configuration of the apparatus to be used so that the temperature of the cleaning liquid and the film temperature of the portion to which the cleaning liquid is applied are in the range of 40° C. to 150° C., respectively.
- the cleaning liquid As a method of applying the cleaning liquid to the film, it can be done by immersing the film with the coating in the cleaning liquid stored in the liquid tank. Alternatively, without using a liquid bath, the required amount of cleaning liquid may be sprayed onto the coated film, or if the cleaning liquid is water, steam may be blown. Moreover, as long as the cleaning liquid can be applied to the coating, it may be sprayed onto the coated film regardless of whether it is on one side or both sides.
- the peeling means may be any method such as bringing a rotating brush into contact with the film, scraping off the film by bringing a member having ridges into continuous contact with the film, or blowing off the film with an air nozzle.
- the water-soluble resin can be dissolved in a short time, so the film can be peeled off at high speed without enlarging the liquid tank or increasing the amount of waste liquid.
- a preferred embodiment of the apparatus for peeling a coating from a film with a coating (hereinafter referred to as a coating peeling apparatus) of the present invention will be described with reference to the drawings. It should be noted that the following description exemplifies an embodiment according to the present invention, and is not limited to this, and various modifications can be made without departing from the gist of the present invention.
- FIG. 1 is a schematic diagram of a coating stripping device 101 according to the first embodiment of the present invention.
- the coating stripping device 101 includes an unwinding device 4 for unwinding the film 2 with the coating and a winding device 5 for winding the base film 3 after stripping the coating. Between the unwinding device 4 and the winding device 5, a coating damage mechanism 6 for damaging the coating from the coated surface 2a of the coated film 2 and a coating damage mechanism 6 for damaging the coated film 2 are provided. It comprises a cleaning liquid application mechanism 10 for applying the cleaning liquid 7 and a peeling mechanism 11 for peeling the coating containing the cleaning liquid 7 from the coated film 2 to which the cleaning liquid 7 has been applied.
- the coated film 2 shown in FIG. 1 has a coating formed on one side of the film, and the coating damage mechanism 6 is installed facing the surface 2a on which the coating is formed.
- the coating damage mechanism 6 may be provided facing each coating surface.
- the cleaning liquid application mechanism 10 includes a liquid tank 8 for storing the cleaning liquid 7 and a pump 9 for feeding the cleaning liquid 7 from a tank (not shown), and conveys the coated film 2 while being immersed in the cleaning liquid 7 in the liquid tank 8. Thus, the cleaning liquid 7 is continuously applied to the coated film 2 .
- the cleaning liquid application mechanism 10 may be any mechanism such as a spray or a nozzle as long as it can apply the cleaning liquid 7 to the film.
- the coated film 2 unwound from the unwinding device 4 is conveyed by a conveying mechanism consisting of driving devices 12a and 12b, and the coating is damaged by the coating damage mechanism 6 before the cleaning liquid 7 is applied by the cleaning liquid applying mechanism 10. be injured.
- the coating damage mechanism 6 is composed of a brush roll.
- a brush roll capable of scratching the film efficiently, the surface of the film can be scraped to scratch it, and the effect of removing the film can also be expected.
- the brush roll can continuously scratch the coating by conveying the film 2 with the coating without rotating. In order to make more scratches, it is preferable to rotate the brush. The higher the number of revolutions, the more the bristles of the brush come into contact with the film, and the more scratches are produced. Further, when the brush roll is rotated, shavings of the coating caused by damage to the coating are not kept in one place and are discharged, which is preferable.
- the direction of rotation of the brush roll may be the same or opposite to the direction of transport of the coated film 2. Any method may be used, and there is no particular limitation as long as the film is damaged.
- the material of the bristles of the brush roll may be appropriately selected from resin, metal, animal hair, plant fiber, etc., and is not particularly limited as long as it can scratch the film, but the material should be harder than the film. can be easily scratched.
- the bristles are preferably fine and dense, allowing more wounds to be made.
- the coating damage mechanism 6 it is possible to use a roller or the like having unevenness on the cylindrical surface, and the coating can be scratched by rubbing.
- the surface of a roller or a round bar is knurled, or that an uneven shape is formed by etching or engraving.
- the stripping mechanism 11 consists of a brush roll similar to that used in the coating damage mechanism 6.
- the peeling mechanism 11 has a mechanism for rotating a brush roll made of metal or resin in the same or opposite direction as the conveying direction, and directly contacts the surface of the coated film 2 to peel off the cleaning liquid and the coating.
- a metal plate with a sharp tip that directly contacts the coated film 2 may be provided, or a resin plate may be provided.
- a thin metal plate may be provided.
- a waste cloth or cloth may be pressed against the coated film 2 and peeled off by wiping off the coated film, or may be blown off with an air nozzle.
- a structure may be added after the peeling mechanism 11 for rinsing, in which a clean cleaning liquid containing no impurities such as foreign matter is sprayed and dried with an air nozzle.
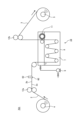
- FIG. 2 is a schematic diagram of a film stripping device 201 according to a second embodiment of the present invention.
- a backup roll 61 is provided at a position facing the brush roll of the coating damage mechanism 6 provided in the first embodiment, with the coated film 2 sandwiched therebetween. is.
- the brush roll can be reliably brought into contact with the coated film 2, which is preferable.
- the material of the bristles of the brush roll harder than the base film 3, the film can be penetrated and scratched including a part of the base film, so that the thickness of the film can be increased. Scratches can be applied in all directions.
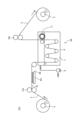
- FIG. 3 is a schematic diagram of a coating stripping device 301 according to a third embodiment of the present invention.
- FIG. 4 is a schematic top view of the coating damage mechanism 6A of FIG.
- a plurality of cutters 62 are provided in the width direction as a coating damage mechanism 6A, and cuts 63 are provided in the coating. is to be inserted. 4
- the coating damage mechanism 6A is observed through the coated film 2, and the coating damage mechanism 6A and the notch 63 are not actually visible, so the cutter 62 and the notch 63 are illustrated with chain lines. .
- the cutter 62 can be lightly applied to the surface 2a on which the coating is formed, without penetrating the base film.
- a notch 63 can be made. It is also possible to cut not only the coating but also a part of the base film by adjusting the amount of pressing of the cutter 62 against the coating and the transport tension of the film 2 with the coating.
- the number of cuts 63 is determined by the number of cutters 62 and the pitch at which they are arranged.
- the cutter 62 may be a rotating round blade, or may be brought into contact with a sharp member having a sharp tip.
- the material of the cutter 62 is not particularly limited as long as it is made of metal, ceramic, resin, or the like and has a sharp tip.
- FIG. 5 is a schematic diagram of a film stripping device 401 according to a fourth embodiment of the invention.
- FIG. 6 is a schematic top view of the coating damage mechanism 6B of FIG.
- the amount of pressing of the cutter 62 of the coating damage mechanism 6A provided in the third embodiment is increased to cut through the base film. , incisions are made in the entire thickness direction of the film.
- the coating peeling apparatus 401 when the coated film 2 is immersed in the cleaning liquid 7 stored in the liquid tank 8 of the cleaning liquid applying mechanism 10, the cleaning liquid 7 passes through the notch 63 of the base film to the surface 2a on which the coating is formed and the surface 2a. Since the film is also applied from the surface 2b without the film, the water-soluble resin can be efficiently dissolved.
- the cleaning liquid application mechanism 10 When the cleaning liquid application mechanism 10 is configured to spray using a spray or the like, the cleaning liquid may be sprayed only from the surface 2a on which the film is formed, or preferably from both surfaces of the film 2 with the film. As in the case of immersion in the cleaning liquid 7 stored in the bath 8, the water-soluble resin can be efficiently dissolved.
- the cleaning liquid 7 when coatings are formed on both sides of the film and the cleaning liquid 7 is applied by spraying using a sprayer or the like, the cleaning liquid spreads over the coating through the cuts in the base film.
- the water-soluble resin can be dissolved as the application, it is more preferable to apply from both sides to efficiently dissolve the water-soluble resin.
- FIG. 7 is a schematic diagram of a film stripping device 501 according to a fifth embodiment of the present invention.
- a roller 64 having sharp protrusions on the cylindrical surface is brought into contact with the coating to form holes in the coating. It is something to do. By rotating the roller 64 at the same peripheral speed as the conveying speed of the coated film 2, it is possible to form holes having substantially the same shape as the protrusions formed on the surface. When the roller 64 is not rotated, a cut similar to that of the cutter of the third embodiment can be made.
- holes extending in the transport direction can be formed according to the peripheral speed difference.
- the shape of the hole is not particularly limited, and may be any shape such as a round hole, an elongated hole, or a polygonal hole.
- the sharp protrusions of the roller 64 can be realized, for example, by planting a needle-like member such as a pincushion on the surface of the cylinder, or by forming sharp protrusions on the surface of the cylinder by laser engraving or machining.
- the thickness of the coating is formed thinner than the thickness of the base film, so simply by pressing the roller 64 lightly against the surface of the coating, holes are formed in the coating without penetrating the base film. Is possible. It is also possible to form a hole that reaches not only the coating but also a part of the base film by adjusting the pressing amount of the roller 64 against the coating and the transport tension of the film 2 with the coating.
- the number of holes is determined by the number of projections and the pitch of the arrangement, so it can be adjusted as appropriate to obtain the desired holes.
- the material of the protrusions is not particularly limited as long as metal, ceramic, resin, or the like can be used, and at least holes can be formed in the film.
- FIG. 8 is a schematic diagram of a coating stripping device 601 according to the sixth embodiment of the present invention.
- the pressing amount of the roller 64 having sharp protrusions on the cylindrical surface of the fifth embodiment shown in FIG. 7 is increased to penetrate the base film.
- a hole is formed to form a hole in the entire thickness direction of the film.
- FIG. 9 is a schematic diagram of a film stripping device 701 according to a seventh embodiment of the invention.
- FIG. 10 is a schematic top view of the coating damage mechanism 6E of FIG.
- the cutter 62 provided in the third embodiment is provided on the side of the surface 2b where the coating is not formed, and penetrates the base film to cut into the coating. be.
- the cleaning solution 7 may not reach the details. There is In that case, if the surface 2b of the base film 2 with the coating is not formed with a scratch, the coating is pushed away from the base film, so there is no possibility that the coating will be buried in the base film. Therefore, it is preferable.
- FIG. 11 is a schematic diagram of a film stripping device 801 according to the eighth embodiment of the present invention.
- FIG. 12 is a schematic top view of the coating damage mechanism 6F of FIG.
- a roller 64 having sharp projections on the cylindrical surface provided in the sixth embodiment is provided on the side of the surface 2b where the film is not formed, and penetrates the base film. to form a hole 67 in the coating.
- the same functions and effects as those of the seventh embodiment described above are exhibited.
- FIG. 13 is a schematic diagram of a film stripping device 901 according to the ninth embodiment of the present invention.
- FIG. 14 is a schematic top view of the coating damage mechanism 6G of FIG.
- a coating damage mechanism 6G of the ninth embodiment has a sharp projection or a sharpened protrusion or a blade-shaped member 65 provided with a plurality of cutters, and a moving means (not shown) for the member 65 .
- the coating damage mechanism 6G is provided on the side of the surface 2a on which the coating is formed.
- a notch 62 is formed in a part of the material film in the thickness direction.
- ⁇ which is an angle (acute angle) formed by the longitudinal direction of the cut 62 and the transport direction
- ⁇ is preferably 60 degrees or less.
- a force obtained by multiplying the applied tension by sin ⁇ that is, a force of 87% or more of the tension acts on the cut 62 at right angles.
- the base film may be stretched or broken.
- the angle ⁇ is preferably 60° or less.
- FIG. 15 is a schematic diagram of the coating stripping device 111 of the tenth embodiment of the present invention.
- FIG. 16 is a schematic top view of the coating damage mechanism 6 of FIG.
- the coating damage mechanism 6H instead of the blade-shaped member 65 provided with a plurality of sharp projections or cutters in the ninth embodiment, a band-shaped brush 66 is brought into contact with the coating to scrape it. , and a wound 68 is made.
- the brush 66 is repeatedly moved back and forth while conveying the film 2 with the film, so that a scratch 68 oblique to the conveying direction can be made.
- ⁇ which is the angle (acute angle) formed by the longitudinal direction of the scratch 68 and the transport direction, be 60 degrees or less.
- a plurality of film damage mechanisms 6 to 6H shown in the first to tenth embodiments may be provided in the film transport direction.
- By providing a plurality of coating damage mechanisms 6 to 6H it becomes possible to form more scratches, cuts, and holes, and further high-speed peeling of the coating can be expected. It is also effective when the composition and thickness of the film make it difficult for the water-soluble resin to dissolve.
- the coating stripping method and the coating stripping apparatus of the present invention the coating can be stripped at high speed by dissolving the water-soluble resin from the surface of the coated film using the cleaning liquid in a short period of time. As a result, it is possible to obtain high-purity resin chips free of foreign matter at low cost without significantly increasing the environmental load.
- a film of polyvinyl alcohol resin having a thickness of 0.1 ⁇ m was formed as a layer containing a water-soluble resin on a base film made of polyethylene terephthalate and having a thickness of 30 ⁇ m and a width of 100 mm. Furthermore, a 0.1 ⁇ m-thick film of a curable silicone resin was formed thereon as a layer containing a release component, with reference to the coating material described in JP-A-2015-189226, as follows.
- thermosetting silicone manufactured by Shin-Etsu Chemical Co., Ltd., trade name “KS-847T”: 100 parts by mass
- Platinum catalyst manufactured by Shin-Etsu Chemical Co., Ltd., trade name “CAT-PL-50T”: 3 parts by mass Coating material Dissolves the above thermosetting silicone and platinum catalyst in a mixture of toluene and MEK as a solvent (toluene:MEK mass ratio is 1:1) so that the solid content is 1.8% by mass. It was prepared by Next, the coating material was applied on the polyvinyl alcohol resin film using a bar coater and dried in an oven at 90° C. for 20 seconds to form a release component film, thereby obtaining film a with a film.
- a film of polyvinyl alcohol resin having a thickness of 0.1 ⁇ m was formed as a layer containing a water-soluble resin on a base film made of polyethylene terephthalate and having a thickness of 30 ⁇ m and a width of 100 mm. Further thereon, as a layer containing a release component, a film of a resin containing a compound having a long-chain alkyl group with a film thickness of 0.1 ⁇ m is formed with reference to the coating material described in JP-A-2019-137005, as follows.
- a coating material is applied on the polyvinyl alcohol resin film using a gravure coater, pre-dried at 100° C., and then dried by heating at 160° C. to form a film of a release component, to obtain a film b with a film. Obtained.
- a film of polyvinyl alcohol resin having a thickness of 0.1 ⁇ m was formed as a layer containing a water-soluble resin on a base film made of polyethylene terephthalate and having a thickness of 30 ⁇ m and a width of 100 mm. Furthermore, a 0.1 ⁇ m-thick curable silicone resin film was formed thereon as a layer containing a release component, with reference to the coating material described in International Publication No. 2013/145864, as follows.
- release agent solution solid content: 20 mass%.
- This release agent solution was applied onto the polyvinyl alcohol resin film by a bar coater so that the thickness after curing was 0.97 ⁇ m, and dried at 80° C. for 1 minute. Thereafter, ultraviolet rays were irradiated (accumulated light quantity: 250 mJ/cm 2 ) to cure the release agent composition to form a coating of the release component, thereby obtaining a coated film c.
- Peelability of Coating Evaluation of peeling was measured by the following method using a commercially available dyne pen (surface energy: 30, 70 mN/m). It was determined that the surface energy of the sample surface was higher than the surface energy of the dyne pen when drawing was made on the sample surface with a dyne pen at room temperature of 23° C. and the state was maintained for 4 seconds or longer. If the coating of the release component of the coated films a to c remains on the surface, the surface energies of these are both less than 30 mN/m, so the reagent is repelled by the sample surface in any of the dyne pens, and the drawing cannot be retained.
- the surface energy is 70 mN/m or more, so any dyne pen can hold the drawing.
- the surface energy is 43.8 mN / m, so the Dyne pen of 30 mN / m
- the drawing is retained, but the dyne pen drawing of 70 mN/m cannot be retained.
- the intrinsic viscosity IV(R) of the sheet obtained in (i) above is measured.
- [ ⁇ ] (dl/g) is calculated by the following formula (a), and the obtained value is defined as the intrinsic viscosity.
- Example 1 As the coated film 2, the coated film a in which the coating was formed on one side of the substrate film was used, and set in the unwinding device 4 of the peeling device 101 shown in FIG.
- the film damage mechanism 6 used a brush roll, which was rotated at 500 rpm in the opposite direction to the film conveying direction, and brought into contact with the film surface to scratch and damage it.
- the bristles of the brush roll are made of nylon resin and have a wire diameter of 0.15 mm. Hot water of 60° C. was used as the cleaning liquid 7 .
- the cleaning liquid applying mechanism 10 has a cleaning liquid 7 stored in a liquid tank 8, and the coated film 2 is introduced into the liquid tank 8, and the film of the polyvinyl alcohol resin is dissolved while being immersed and transported in the cleaning liquid 7.
- the length of the coated film 2 immersed in the cleaning solution 7 was 0.5 m.
- the transport tension of the film was 60 N, and the transport speed was 50 m/min. Therefore, the time during which the coated film 2 is in contact with the cleaning liquid 7 is 0.6 seconds.
- the peeling mechanism 11 used a metal brush roll, which was rotated at 500 rpm in the opposite direction to the film conveying direction, and brought into contact with the surface of the film to peel the film.
- the substrate film 3 was wound by the winding device 5, the coating was peeled off, and the base film 3 was sampled.
- the peeled state of the coating was checked with a dyne pen, it was found that the curable silicone resin and the water-soluble polyvinyl alcohol resin as release components were mixed. It was confirmed that all the films were peeled off.
- a polyethylene terephthalate film was obtained without bubbles, gels, or the like in the molten polymer, and without any abnormalities such as pressure rise.
- the difference in intrinsic viscosity was 0.03, and it was confirmed that the quality of the recycled resin chips was within the acceptable range.
- Example 2 A coated film a in which a coating was formed on one side of a substrate film was used as the coated film 2 and set in the unwinding device 4 of the peeling device 901 shown in FIG. 13 .
- the film damage mechanism 6G uses a member 65 in which a plurality of stainless steel wires with a diameter of 1 mm are arranged at a pitch of 3 mm as sharp projections, is brought into contact along the film surface, and is reciprocated in the film width direction at a speed of 50 m / min. An incision 62 was made in the coating. As a result, the angle (acute angle) between the longitudinal direction of the slit 62 and the conveying direction was 45 degrees.
- a polyethylene terephthalate film was obtained without bubbles, gels, or the like in the molten polymer, and without any abnormalities such as pressure rise.
- the difference in intrinsic viscosity was 0.05, and it was confirmed that the quality of the recycled resin chips was within a satisfactory range.
- Example 3 Film b obtained by forming a coating on one side of a substrate film was used as film 2 with coating, and peeling was performed using the peeling apparatus 101 of Example 1 under the same conditions as in Example 1.
- the base film 3 was wound up by the winding device 5, and the base film 3 from which the coating had been peeled off was sampled. It was confirmed that all the films of the poly(vinyl alcohol) resin could be peeled off.
- a polyethylene terephthalate film was produced in the same manner as in Example 1 using recycled resin chips. A polyethylene terephthalate film was obtained without bubbles, gels, or the like in the molten polymer, and without any abnormalities such as pressure rise. The difference in intrinsic viscosity was 0.04, and it was confirmed that the quality of the recycled resin chips was within a satisfactory range.
- Example 4 Using the coated film c in which the coated film was formed on one side of the base film as the coated film 2, the peeling apparatus 101 of Example 1 was used to peel the film.
- the brush roll of the coating damage mechanism 6 was rotated at 1500 rpm in the opposite direction to the film conveying direction, and brought into contact with the coating surface to scratch and damage it. Other conditions were the same as in Example 1.
- the substrate film 3 was wound by the winding device 5, the coating was peeled off, and the base film 3 was sampled. When the peeled state of the coating was checked with a dyne pen, it was found that the curable silicone resin and the water-soluble polyvinyl alcohol resin as release components were mixed. It was confirmed that all the films were peeled off.
- a polyethylene terephthalate film was produced in the same manner as in Example 1 using recycled resin chips.
- a polyethylene terephthalate film was obtained without bubbles, gels, or the like in the molten polymer, and without any abnormalities such as pressure rise.
- the difference in intrinsic viscosity was 0.05, and it was confirmed that the quality of the recycled resin chips was within a satisfactory range.
- Example 1 A coated film a in which a coating was formed on one side of a substrate film was used as the coated film 2, and peeling was performed using the peeling device 101 of FIG. Other conditions were the same as in Example 1, and the coating was peeled off.
- the substrate film 3 was wound by the winding device 5, the coating was peeled off, and the base film 3 was sampled.
- the peeled state of the coating was checked with a dyne pen, it was found that the curable silicone resin and the water-soluble polyvinyl alcohol resin as release components were mixed. It was confirmed that part of the coating remained.
- a polyethylene terephthalate film was produced using the recycled resin chips in the same manner as in Example 1, and it was confirmed that air bubbles were mixed in the molten polymer. In addition, it was confirmed that the produced polyethylene terephthalate film had a difference of 0.23 in intrinsic viscosity, and the quality of the recycled resin chips could not withstand practical use.
- the method and device for peeling the coating from the coated film of the present invention are not limited to the film having the coating containing the water-soluble resin on one side of the base film, and the recycling having the coating containing the easily soluble resin layer. It can also be applied as a method and device for peeling coatings from resin films, paper films, and metal films.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Environmental & Geological Engineering (AREA)
- Mechanical Engineering (AREA)
- General Chemical & Material Sciences (AREA)
- Medicinal Chemistry (AREA)
- Health & Medical Sciences (AREA)
- Sustainable Development (AREA)
- Polymers & Plastics (AREA)
- Organic Chemistry (AREA)
- Life Sciences & Earth Sciences (AREA)
- Application Of Or Painting With Fluid Materials (AREA)
- Laminated Bodies (AREA)
- Separation, Recovery Or Treatment Of Waste Materials Containing Plastics (AREA)
- Cleaning In General (AREA)
Abstract
Description
また近年、IoT(Internet of Things)の進化により、コンピュータやスマートフォンに搭載されるCPUなどの電子デバイスが増加し、それに伴い、電子デバイスを駆動するために必要な積層セラミックコンデンサー(MLCC)の数も急激に増加している。このMLCCの一般的な製造方法は、プラスチックの基材フィルム上に離型層を形成した離型フィルムをキャリアシートとして使用し、その離型フィルム上にセラミックグリーンシート層を形成する工程と、そのセラミックグリーンシート層を剥離してセラミックグリーンシートとする工程がある。
廃棄された離型フィルムを再利用するには、回収/粉砕/樹脂チップにした後、再溶融して製膜を行うことで再生フィルムを得ればよい。
しかし、離型フィルムに含まれる離型層の成分は、離型性の観点から、一般的には基材フィルムを構成する成分とは異なる組成であるため、離型層が付いた離型フィルムを粉砕し、樹脂チップにした後、再溶融して製膜すると、離型層の成分が異物として存在するため、安定製膜をすることが困難となる。
したがって、離型フィルムを再生フィルムとしてリサイクルするためには、離型フィルムに含まれる離型層の成分を再生フィルムの品質として問題ないレベルの極微量の残渣にまで除去することが必要である。そして、回収/粉砕/高純度の樹脂チップを得た後、再溶融して再生フィルムとしてリサイクルすることを長期間にわたり、低コストで循環させることが望まれる。
処理速度を上げながら温液槽内で2秒以上接触させるためには、温液槽を大型化して、パス長を稼ぐことが必要となり、非現実的なサイズまでに大型化した温液槽が必要となる。さらに、温液槽が大型化することで、水溶性樹脂層が溶解した廃液量が増大して、処理コストが大幅に高くなるだけでなく、環境負荷が著しく大きくなる、という問題がある。
[2]上記[1]の被膜の剥離方法は、上記被膜付きフィルムを搬送しながら、上記傷を、傷の長手方向と搬送方向との成す角度(鋭角)が60度以下となるようにつける、または、上記切れ込みを、切れ込みの長手方向と搬送方向との成す角度(鋭角)が60度以下となるように入れることが好ましい。
[3]上記[1]または[2]の被膜の剥離方法は、上記被膜が水溶性樹脂を含むことが好ましい。
[4]上記[1]~[3]のいずれかの被膜の剥離方法は、上記被膜が硬化型シリコーン樹脂を含むことが好ましい。
[5]上記[1]~[4]のいずれかの被膜の剥離方法は、上記洗浄液が水であることが好ましい。
[6]上記課題を解決する本発明の被膜の剥離装置は、基材フィルムの少なくとも片面に被膜を有する被膜付きフィルムからの被膜の剥離装置であって、上記被膜付きフィルムの上記被膜のある面から被膜に傷をつける、切れ込みを入れる、もしくは穴を形成する、または、上記被膜付きフィルムの上記被膜の無い面から被膜に達する傷をつける、切れ込みを入れる、もしくは穴を形成する被膜損傷機構と、
上記傷がついた、上記切れ込みが入った、または上記穴が形成された上記被膜付きフィルムの上記被膜に洗浄液を付与する洗浄液付与機構と、
上記被膜付きフィルムから上記洗浄液を含んだ被膜を剥離する剥離機構と、
を備えている。
[7]上記[6]の被膜の剥離装置は、上記被膜付きフィルムを搬送する搬送機構を備え、上記被膜損傷機構が、上記傷を、傷の長手方向と搬送方向との成す角度(鋭角)が60度以下となるようにつける、または、上記切れ込みを、切れ込みの長手方向と搬送方向との成す角度(鋭角)が60度以下となるように入れることが好ましい。
[8]上記[6]または[7]の被膜の剥離装置は、ロール状に巻かれている上記被膜付きフィルムを巻き出すための巻出装置と、上記被膜が剥離された上記基材フィルムを巻き取るための巻取装置と、を備えてもよい。
本発明の被膜付きフィルムの被膜剥離方法は、基材フィルムの表面に被膜を有する被膜付きフィルムを対象として、被膜を洗浄して基材フィルムから被膜を剥離して取り除く方法である。被膜は、基材フィルムの片面にあっても両面にあってもよく、特に限定されない。
対象となる被膜付きフィルムの被膜は、あらゆる組成の被膜が対象となり得るが、中でも環境への負荷等を考慮した水溶性樹脂を含む被膜が好ましい。水溶性樹脂として、水溶性のポリエステル系樹脂、ポリエステルウレタン系樹脂、アクリル系樹脂、エチレンアイオノマー系樹脂、ポリビニルアルコール系樹脂、ポリビニルピロリドン系樹脂、エチレン-ビニルアルコール系樹脂、でんぷんのうちの少なくとも1種を主たる成分とするものがより好ましい。
本発明の被膜付きフィルムからの被膜の剥離方法(以下、被膜剥離方法とする)は、被膜付きフィルムの被膜のある面から被膜に傷をつけ、切れ込みを入れ、もしくは穴を形成し、または、被膜付きフィルムの被膜の無い面から被膜に達する傷をつけ、切れ込みを入れ、もしくは穴を形成し、次いで、被膜に洗浄液を接触させ、次いで、被膜付きフィルムから洗浄液を含んだ被膜を剥離する。すなわち、被膜に洗浄液を接触させる前に、被膜に傷をつけ、切れ込みを入れ、または穴を形成することで被膜に損傷を与えることに特徴があり、被膜に効率よく洗浄液を浸透させ、短時間で被膜を溶解させる。
本発明の被膜付きフィルムからの被膜の剥離装置(以下、被膜剥離装置とする)の望ましい実施形態について、図面に基づいて説明する。なお、以下の説明は本発明に係る実施形態を例示するものであり、これに限定されるものではなく、本発明の趣旨を逸脱しない範囲で種々の変更が可能である。
被膜付きフィルム2の搬送張力が小さい場合や、ブラシロールが高速回転する場合、被膜付きフィルム2がブラシロールの反対側へ押しやられる力が働き、微小な周期で被膜付きフィルム2が浮上することで、ブラシロールと被膜付きフィルム2との接触力が不足して傷の数や深さが減少することがある。そのため、バックアップロール61を設けて被膜付きフィルム2の浮上を防止することで、確実にブラシロールを被膜付きフィルム2に接触できるので好ましい。
このとき、ブラシロールの毛の材質を基材フィルム3より高硬度にすることで、被膜を貫通して、基材フィルムの一部を含めて傷を入れられることから、より確実に被膜の厚み方向全域に対して、傷を入れることができる。
カッター62は、回転丸刃であってもよいし、先端の尖った鋭利な部材を接触させてもよい。
カッター62の材質は、金属やセラミック、樹脂などを使用し、先端を鋭利に加工したものであれば特に限定するものではない。
被膜剥離装置401では、被膜付きフィルム2を洗浄液付与機構10の液槽8に貯めた洗浄液7に浸漬した際、洗浄液7が、基材フィルムの切れ込み63を通じて、被膜が形成されている面2aおよび被膜の無い面2bからも付与されることになるので、効率よく水溶性樹脂の溶解を行うことができる。
ローラー64は、被膜付きフィルム2の搬送速度と同じ周速で回転させることで、表面に形成した突起形状と略同一形状の穴を形成することができる。ローラー64を回転させない場合は、第3の実施形態の、カッターと同様な切れ込みを入れることができる。また、ローラー64を搬送速度と異なる周速で回転、または、搬送方向に対して逆回転させると、周速差に応じて搬送方向に伸びる穴を形成することができる。穴の形状は、特に限定するものではなく、丸穴や長穴、多角形穴などいかなる形状であっても良い。
基材フィルムや被膜の物性や組成、基材フィルムと被膜の界面の状態によっては、傷を入れた際、被膜の一部が基材フィルムに埋没して、洗浄液7が細部まで行きわたらない場合がある。その場合、被膜付き基材フィルム2の被膜が形成されていない面2b側から傷を入れれば、被膜が基材フィルムから離れる方向へ押しやられるので、被膜が基材フィルム中に埋没するおそれがなくなるため好ましい。
フィルムの搬送時は、張力をかけているが、角度θが60度を超えると、付与している張力にsinθを乗じた力、すなわち、張力の87%以上の力が切れ込み62に直角に作用することになり、大きな張力をかけていると、基材フィルムの伸びや破断につながる恐れがある。特に基材フィルムの厚み方向の一部に達する切れ込み62がある場合、フィルム伸びや破断が発生しやすくなるため、角度θは60°以下とすることが好ましい。
以下に示す、3種類の被膜付きフィルムを作製した。
ポリエチレンテレフタレートからなる厚み30μm、幅100mmの基材フィルム上に、水溶性樹脂を含む層として膜厚0.1μmのポリビニルアルコール樹脂の被膜を形成した。
さらにその上に、離型成分を含む層として膜厚0.1μmの硬化型シリコーン樹脂の被膜を、特開2015-189226号公報に記載の塗材を参考にして、以下のように形成した。
使用材料
・熱硬化型シリコーン、信越化学工業社製、商品名「KS-847T」:100質量部
・白金触媒、信越化学工業社製、商品名「CAT-PL-50T」:3質量部
塗材は、上記の熱硬化性シリコーンおよび白金触媒を、溶剤としてのトルエンとMEKの混合液(トルエン:MEKの質量比は1:1)中に、固形分が1.8質量%となるように溶解させることで調製した。次に前記ポリビニルアルコール樹脂の被膜上に、塗材をバーコーターを用いて塗布し、90℃のオーブンで20秒乾燥させて離型成分の被膜を形成し、被膜付きフィルムaを得た。
ポリエチレンテレフタレートからなる厚み30μm、幅100mmの基材フィルム上に、水溶性樹脂を含む層として膜厚0.1μmのポリビニルアルコール樹脂の被膜を形成した。
さらにその上に、離型成分を含む層として膜厚0.1μmの長鎖アルキル基を有する化合物を含む樹脂の被膜を、特開2019-137005号公報に記載の塗材を参考にして、以下のように形成した。
使用材料
・長鎖アルキル基含有化合物、ライオン・スペシャリティ・ケミカルズ社製、商品名「ピーロイル」1050:固形分換算で10質量部
・架橋剤、住友化学社製、商品名「スミマール」M-55:固形分換算で2.5質量部
・酸触媒、テイカ社製、商品名「TAYCACURE」AC-700:固形分換算で1.3質量部
・溶剤、トルエン400質量部、MEK130質量部
塗材は、上記の長鎖アルキル基含有化合物、架橋剤、酸触媒を、溶剤に溶解して調整した。次に前記ポリビニルアルコール樹脂の被膜上に、塗材をグラビアコーターを用いて塗布し、100℃で予備乾燥後、160℃で加熱乾燥させて離型成分の被膜を形成し、被膜付きフィルムbを得た。
ポリエチレンテレフタレートからなる厚み30μm、幅100mmの基材フィルム上に、水溶性樹脂を含む層として膜厚0.1μmのポリビニルアルコール樹脂の被膜を形成した。
さらにその上に、離型成分を含む層として膜厚0.1μmの硬化型シリコーン樹脂の被膜を、国際公開第2013/145864号に記載の塗材を参考にして、以下のよう形成した。
使用材料
・活性エネルギー線硬化性成分、ジペンタエリスリトールヘキサアクリレート、新中村工業社製,商品面「A-DPH」固形分100質量%:99.0質量部
・シリコーン系成分、ポリエーテル変性アクリロイル基含有ポリジメチルシロキサン、ビッグケミー社製,商品名「BYK-3500」固形分100質量%:1.0質量部
・光重合開始剤である2-メチル-1[4-(メチルチオ)フェニル]-2-モルフォリノプロパン-1-オン、BASF社製,商品名「IRGACURE907」:5.0質量部
塗材は、上記のジペンタエリスリトールヘキサアクリレート、ポリエーテル変性アクリロイル基含有ポリジメチルシロキサン、光重合開始剤を、イソプロピルアルコールおよびメチルエチルケトンの混合液(混合質量率3:1)にて希釈して、これを離型剤溶液(固形分20質量%)とした。この離型剤溶液を、バーコーターにより前記ポリビニルアルコール樹脂の被膜上に、硬化後の厚さが0.97μmとなるように塗布し、80℃で1分間乾燥させた。その後、紫外線を照射(積算光量:250mJ/cm2)し、離型剤組成物を硬化させて離型成分の被膜を形成し、被膜付きフィルムcを得た。
(1)被膜の剥離性
剥離の評価は、市販のダインペン(表面エネルギー:30、70mN/m)を用いて、以下の方法で測定した。室温23℃の環境下で、試料表面にダインペンで描画し、4秒以上その状態を保持する場合は、そのダインペンの表面エネルギーよりも試料表面の表面エネルギーの方が高いと判断した。被膜付きフィルムa~cの離型成分の被膜が表面に残れば、これらの表面エネルギーはともに30mN/m未満であるため、いずれのダインペンも試料表面に試薬が弾かれて、描画を保持できない。一方、離型成分の被膜が剥離されて、ポリビニルアルコール樹脂が表出している場合には、表面エネルギーが70mN/m以上であるため、いずれのダインペンも描画を保持できる。離型成分の被膜と水溶性のポリビニルアルコール樹脂の被膜がいずれも剥離されて、ポリエチレンテレフタレートが表出している場合には、表面エネルギーが43.8mN/mであるため、30mN/mのダインペンの描画は保持するが、70mN/mのダインペンの描画は保持できない。以上の評価方法により、被膜付きフィルムの被膜が剥離できたか否かを判断した。
(i)溶融製膜性
被膜付きフィルムから被膜を剥離した後、基材フィルムを回収する。回収した基材フィルムをクラッシャーで粉砕した後、造粒機で造粒した再生樹脂チップを、180℃で2時間乾燥した後、押出機に投入し280℃で溶融押出して、25℃に冷却したキャストドラム上でシート状に成形し、問題なくポリエチレンテレフタレートフィルムが作製できるか否かを確認する。
上記(i)で得られたシートの固有粘度IV(R)を測定する。固有粘度IV(R)は、オルトクロロフェノール100mlにポリエチレンテレフタレートフィルムを溶解させ(溶液濃度C=1.2g/dl)、その溶液の25℃での粘度を、オストワルド粘度計を用いて測定する。また、同様に溶媒の粘度を測定する。得られた溶液粘度、溶媒粘度を用いて、下記(a)式により、[η](dl/g)を算出し、得られた値でもって固有粘度とする。
(a)ηsp/C=[η]+K[η]2・C
(ここで、ηsp=(溶液粘度(dl/g)/溶媒粘度(dl/g))―1、Kはハギンス定数(0.343とする)である。)
次に、被膜付きフィルムを作製する前に、あらかじめサンプリングしておいた被膜を形成する前の基材フィルムの固有粘度IV(I)を同様に測定する。
異物の混入などによって生じる樹脂チップの品質低下は、IV(R)とIV(I)の差として表れるので、下記(b)式により、ΔIVを算出し、得られた値でもって以下のように判定する。
(b)ΔIV=IV(R)-IV(I)
・固有粘度の差が0.05以下:再生樹脂チップの品質として問題ない範囲にある。
・固有粘度の差が0.05を超えて0.2未満:再生樹脂チップの品質としてやや劣るものの、実用の範囲内にある。
・固有粘度の差が0.2を超える:再生樹脂チップの品質として実用に耐えられない。
被膜付きフィルム2として基材フィルムの片面に被膜が形成された被膜付きフィルムaを使用し、図1に示す剥離装置101の巻出装置4にセットした。
被膜損傷機構6は、ブラシロールを用い、フィルム搬送方向に対して500rpmで逆回転し、被膜表面に接触させて擦過し、傷を入れた。ブラシロールの毛の材質は、ナイロン樹脂製で、線径0.15mmである。
洗浄液7は60℃の温水を用いた。洗浄液付与機構10は、液槽8の中に洗浄液7を貯めたものであり、被膜付きフィルム2を液槽8に導き、洗浄液7中を浸漬搬送させながら、ポリビニルアルコール樹脂の被膜を溶解した。被膜付きフィルム2が洗浄液7に浸漬している長さは0.5mとした。
フィルムの搬送張力は60N、搬送速度は50m/分とした。従って、被膜付きフィルム2が洗浄液7に接触している時間は0.6秒となる。
剥離機構11は、金属製のブラシロールを用い、フィルム搬送方向に対して500rpmで逆回転し、被膜表面に接触させて被膜の剥離を実施した。
巻取装置5で巻き取りを行い、被膜を剥離した基材フィルム3を採取して、ダインペンで被膜の剥離状態を確認したところ、離型成分の硬化型シリコーン樹脂と水溶性のポリビニルアルコール樹脂の被膜がいずれも剥離できていることを確認した。
そして、基材フィルム3を回収した後、クラッシャーで粉砕し、造粒機で樹脂チップにした。その後、押出機に投入し280℃で溶融押出して、25℃に冷却したキャストドラム上でシート状に成形し、ポリエチレンテレフタレートフィルムを作製した。溶融ポリマー中に気泡やゲル等確認されず、圧力上昇などの異常も発生することなく、ポリエチレンテレフタレートフィルムを得ることができた。固有粘度の差は0.03であり、再生樹脂チップの品質として問題ない範囲にあることを確認した。
被膜付きフィルム2として基材フィルムの片面に被膜が形成された被膜付きフィルムaを使用し、図13に示す剥離装置901の巻出装置4にセットした。
被膜損傷機構6Gは、鋭利な突起として直径1mmのステンレス線材を3mmピッチで複数本配置した部材65を用い、被膜表面に沿わせて接触させ、フィルム幅方向へ速度50m/分で往復移動させて被膜に切り込み62を入れた。その結果、切れ込み62の長手方向と搬送方向との成す角度(鋭角)が45度となった。また、切れ込み62は、基材フィルムの一部にまで到達していることが目視により確認できた。その他の条件は、実施例1と同様にして被膜の剥離を行った。
巻取装置5で巻き取りを行い、被膜を剥離した基材フィルム3を採取して、ダインペンで被膜の剥離状態を確認したところ、離型成分の硬化型シリコーン樹脂と水溶性のポリビニルアルコール樹脂の被膜がいずれも剥離できていることを確認した。
そして、基材フィルム3を回収した後、実施例1と同様にして再生樹脂チップを用いてポリエチレンテレフタレートフィルムを作製した。溶融ポリマー中に気泡やゲル等確認されず、圧力上昇などの異常も発生することなく、ポリエチレンテレフタレートフィルムを得ることができた。固有粘度の差は0.05であり、再生樹脂チップの品質として問題ない範囲にあることを確認した。
被膜付きフィルム2として基材フィルムの片面に被膜が形成された被膜付きフィルムbを使用し、実施例1の剥離装置101を用い、実施例1と同様の条件で、剥離を行った。
巻取装置5で巻き取りを行い、被膜を剥離した基材フィルム3を採取して、ダインペンで被膜の剥離状態を確認したところ、離型成分の長鎖アルキル基を有する化合物を含む樹脂と水溶性のポリビニルアルコール樹脂の被膜がいずれも剥離できていることを確認した。
そして、基材フィルム3を回収した後、実施例1と同様にして再生樹脂チップを用いてポリエチレンテレフタレートフィルムを作製した。溶融ポリマー中に気泡やゲル等確認されず、圧力上昇などの異常も発生することなく、ポリエチレンテレフタレートフィルムを得ることができた。固有粘度の差は0.04であり、再生樹脂チップの品質として問題ない範囲にあることを確認した。
被膜付きフィルム2として基材フィルムの片面に被膜が形成された被膜付きフィルムcを使用し、実施例1の剥離装置101を用い、剥離を行った。被膜損傷機構6のブラシロールは、フィルム搬送方向に対して1500rpmで逆回転し、被膜表面に接触させて擦過し、傷を入れた。それ以外の条件は、実施例1と同様にした。
巻取装置5で巻き取りを行い、被膜を剥離した基材フィルム3を採取して、ダインペンで被膜の剥離状態を確認したところ、離型成分の硬化型シリコーン樹脂と水溶性のポリビニルアルコール樹脂の被膜がいずれも剥離できていることを確認した。
そして、基材フィルム3を回収した後、実施例1と同様にして再生樹脂チップを用いてポリエチレンテレフタレートフィルムを作製した。溶融ポリマー中に気泡やゲル等確認されず、圧力上昇などの異常も発生することなく、ポリエチレンテレフタレートフィルムを得ることができた。固有粘度の差は0.05であり、再生樹脂チップの品質として問題ない範囲にあることを確認した。
被膜付きフィルム2として基材フィルムの片面に被膜が形成された被膜付きフィルムaを使用し、被膜損傷機構6であるブラシロール取り外した図1の剥離装置101を用い、、剥離を行った。その他の条件は実施例1と同様にして被膜の剥離を行った。
巻取装置5で巻き取りを行い、被膜を剥離した基材フィルム3を採取して、ダインペンで被膜の剥離状態を確認したところ、離型成分の硬化型シリコーン樹脂と水溶性のポリビニルアルコール樹脂の被膜の一部が残存していることを確認した。
そして、基材フィルム3を回収した後、実施例1と同様にして再生樹脂チップを用いてポリエチレンテレフタレートフィルムを作製したところ、溶融ポリマー中に気泡が混在することを確認した。また、作製したポリエチレンテレフタレートフィルムについて、固有粘度の差は0.23であり、再生樹脂チップの品質として実用に耐えられないものであることを確認した。
2a 皮膜が形成された面
2b 皮膜が形成されていない面
3 基材フィルム
4 巻出装置
5 巻取装置
6、6A、6B、6C、6D、6E、6F、6G、6H 被膜損傷機構
7 洗浄液
8 液槽
9 ポンプ
10 洗浄液付与機構
11 剥離機構
12a、12b 駆動装置
61 バックアップロール
62 カッター
63 切れ込み
64 ローラー
65 部材
66 ブラシ
67 穴
68 傷
101、201、301、401、501、601、701、801、901、111 剥離装置
Claims (8)
- 基材フィルムの少なくとも片面に被膜を有する被膜付きフィルムからの被膜の剥離方法であって、
前記被膜付きフィルムの前記被膜のある面から被膜に傷をつけ、切れ込みを入れ、もしくは穴を形成し、または、前記被膜付きフィルムの前記被膜の無い面から被膜に達する傷をつけ、切れ込みを入れ、もしくは穴を形成し、
次いで、前記被膜に洗浄液を接触させ、
次いで、前記被膜付きフィルムから前記洗浄液を含んだ前記被膜を剥離する、
被膜付きフィルムからの被膜の剥離方法。 - 前記被膜付きフィルムを搬送しながら、
前記傷を、傷の長手方向と搬送方向との成す角度(鋭角)が60度以下となるようにつける、または、前記切れ込みを、切れ込みの長手方向と搬送方向との成す角度(鋭角)が60度以下となるように入れる、
請求項1の被膜付きフィルムからの被膜の剥離方法。 - 前記被膜が水溶性樹脂を含む、請求項1または2の被膜付きフィルムからの被膜の剥離方法。
- 前記被膜が硬化型シリコーン樹脂を含む、請求項1または2の被膜付きフィルムからの被膜の剥離方法。
- 前記洗浄液が水である、請求項3の被膜付きフィルムからの被膜の剥離方法。
- 基材フィルムの少なくとも片面に被膜を有する被膜付きフィルムから被膜を剥離する剥離装置であって、
前記被膜付きフィルムの前記被膜のある面から被膜に傷をつける、切れ込みを入れる、もしくは穴を形成する、または、前記被膜付きフィルムの前記被膜の無い面から被膜に達する傷をつける、切れ込みを入れる、もしくは穴を形成する被膜損傷機構と、
前記傷がついた、前記切れ込みが入った、または前記穴が形成された前記被膜付きフィルムの前記被膜に洗浄液を付与する洗浄液付与機構と、
前記被膜付きフィルムから前記洗浄液を含んだ被膜を剥離する剥離機構と、
を備えた被膜付きフィルムからの被膜の剥離装置。 - 前記被膜付きフィルムを搬送する搬送機構を備え、
前記被膜損傷機構が、前記傷を、傷の長手方向と搬送方向との成す角度(鋭角)が60度以下となるようにつける、または、前記切れ込みを、切れ込みの長手方向と搬送方向との成す角度(鋭角)が60度以下となるように入れる、
請求項6の被膜付きフィルムからの被膜の剥離装置。 - ロール状に巻かれている前記被膜付きフィルムを巻き出すための巻出装置と、
前記被膜が剥離された前記基材フィルムを巻き取るための巻取装置と、
を備えた、請求項6または7の被膜付きフィルムからの被膜の剥離装置。
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2022574723A JPWO2023106002A1 (ja) | 2021-12-09 | 2022-11-01 | |
| US18/713,750 US20250026902A1 (en) | 2021-12-09 | 2022-11-01 | Coating film removing method and coating film removing equipment for removing coating film from coated film |
| CN202280075943.3A CN118251295A (zh) | 2021-12-09 | 2022-11-01 | 从带被膜的膜剥离被膜的方法及被膜的剥离装置 |
| KR1020247012410A KR20240121709A (ko) | 2021-12-09 | 2022-11-01 | 피막 부착 필름으로부터의 피막의 박리 방법 및 피막의 박리 장치 |
| EP22903934.2A EP4446372A4 (en) | 2021-12-09 | 2022-11-01 | METHOD FOR SEPARING A COATING FILM FROM A COATED FILM AND DEVICE FOR SEPArating COATING FILMS |
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2021199776 | 2021-12-09 | ||
| JP2021-199776 | 2021-12-09 | ||
| JP2022-084238 | 2022-05-24 | ||
| JP2022084238 | 2022-05-24 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2023106002A1 true WO2023106002A1 (ja) | 2023-06-15 |
Family
ID=86730206
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2022/040912 Ceased WO2023106002A1 (ja) | 2021-12-09 | 2022-11-01 | 被膜付きフィルムからの被膜の剥離方法および被膜の剥離装置 |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US20250026902A1 (ja) |
| EP (1) | EP4446372A4 (ja) |
| JP (1) | JPWO2023106002A1 (ja) |
| KR (1) | KR20240121709A (ja) |
| TW (1) | TW202337572A (ja) |
| WO (1) | WO2023106002A1 (ja) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20250196198A1 (en) * | 2022-02-24 | 2025-06-19 | Toray Industries, Inc. | Coating film removing equipment and coating film removing method |
| US12629729B2 (en) * | 2022-02-24 | 2026-05-19 | Toray Industries, Inc | Coating film removing equipment and coating film removing method |
Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2000025041A (ja) * | 1998-07-14 | 2000-01-25 | Unitika Ltd | 樹脂フィルムからのコート層の剥離方法 |
| JP2004169005A (ja) * | 2002-11-05 | 2004-06-17 | Toray Ind Inc | 積層フィルムのリサイクル方法およびリサイクル製品 |
| JP2004363140A (ja) * | 2003-06-02 | 2004-12-24 | Toray Ind Inc | 積層フィルムの剥離方法および剥離装置 |
| KR100878986B1 (ko) * | 2007-10-30 | 2009-01-15 | 유영산업주식회사 | 팽윤액을 이용한 필름 접착제분리기 |
| WO2013145864A1 (ja) | 2012-03-28 | 2013-10-03 | リンテック株式会社 | セラミックグリーンシート製造工程用剥離フィルム |
| JP2015189226A (ja) | 2014-03-31 | 2015-11-02 | 三井化学東セロ株式会社 | 離型フィルム |
| JP2019137005A (ja) | 2018-02-15 | 2019-08-22 | 東レフィルム加工株式会社 | 離型フィルム |
| JP2019209511A (ja) * | 2018-05-31 | 2019-12-12 | 日本ゼオン株式会社 | 分離装置、及び、樹脂フィルムの製造方法 |
| JP2021146682A (ja) * | 2020-03-23 | 2021-09-27 | 株式会社ユニチカテクノス | ポリ塩化ビニリデンコーティングフィルムからの熱可塑性樹脂フィルムの回収方法及び回収装置 |
Family Cites Families (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH07148737A (ja) * | 1993-11-29 | 1995-06-13 | Fuji Photo Film Co Ltd | 樹脂被覆紙から紙基材を採取する方法 |
| JP4989617B2 (ja) * | 2008-12-10 | 2012-08-01 | 株式会社 アイワプラスチックス | 剥離再生装置 |
| EP4129675A4 (en) * | 2020-03-31 | 2024-03-06 | Mitsubishi Chemical Corporation | POLYESTER RECYCLING SYSTEM AND METHOD |
-
2022
- 2022-11-01 KR KR1020247012410A patent/KR20240121709A/ko active Pending
- 2022-11-01 EP EP22903934.2A patent/EP4446372A4/en active Pending
- 2022-11-01 JP JP2022574723A patent/JPWO2023106002A1/ja active Pending
- 2022-11-01 WO PCT/JP2022/040912 patent/WO2023106002A1/ja not_active Ceased
- 2022-11-01 US US18/713,750 patent/US20250026902A1/en active Pending
- 2022-12-08 TW TW111147127A patent/TW202337572A/zh unknown
Patent Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2000025041A (ja) * | 1998-07-14 | 2000-01-25 | Unitika Ltd | 樹脂フィルムからのコート層の剥離方法 |
| JP2004169005A (ja) * | 2002-11-05 | 2004-06-17 | Toray Ind Inc | 積層フィルムのリサイクル方法およびリサイクル製品 |
| JP2004363140A (ja) * | 2003-06-02 | 2004-12-24 | Toray Ind Inc | 積層フィルムの剥離方法および剥離装置 |
| KR100878986B1 (ko) * | 2007-10-30 | 2009-01-15 | 유영산업주식회사 | 팽윤액을 이용한 필름 접착제분리기 |
| WO2013145864A1 (ja) | 2012-03-28 | 2013-10-03 | リンテック株式会社 | セラミックグリーンシート製造工程用剥離フィルム |
| JP2015189226A (ja) | 2014-03-31 | 2015-11-02 | 三井化学東セロ株式会社 | 離型フィルム |
| JP2019137005A (ja) | 2018-02-15 | 2019-08-22 | 東レフィルム加工株式会社 | 離型フィルム |
| JP2019209511A (ja) * | 2018-05-31 | 2019-12-12 | 日本ゼオン株式会社 | 分離装置、及び、樹脂フィルムの製造方法 |
| JP2021146682A (ja) * | 2020-03-23 | 2021-09-27 | 株式会社ユニチカテクノス | ポリ塩化ビニリデンコーティングフィルムからの熱可塑性樹脂フィルムの回収方法及び回収装置 |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP4446372A4 |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20250196198A1 (en) * | 2022-02-24 | 2025-06-19 | Toray Industries, Inc. | Coating film removing equipment and coating film removing method |
| US12629729B2 (en) * | 2022-02-24 | 2026-05-19 | Toray Industries, Inc | Coating film removing equipment and coating film removing method |
Also Published As
| Publication number | Publication date |
|---|---|
| EP4446372A4 (en) | 2025-12-03 |
| TW202337572A (zh) | 2023-10-01 |
| KR20240121709A (ko) | 2024-08-09 |
| JPWO2023106002A1 (ja) | 2023-06-15 |
| EP4446372A1 (en) | 2024-10-16 |
| US20250026902A1 (en) | 2025-01-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| TWI913410B (zh) | 從附有被膜之薄膜的被膜剝離方法及被膜剝離裝置 | |
| JP7780579B2 (ja) | ポリエステルフィルムの製造方法、およびポリエステルペレットの製造方法 | |
| CN115362201B (zh) | 聚酯的再循环系统和再循环方法 | |
| KR101766574B1 (ko) | 장척상의 점착 필름 | |
| TWI666304B (zh) | 光學膜之製造方法 | |
| JP2021175812A (ja) | ポリエステルのリサイクルシステム及びリサイクル方法 | |
| CN107709488B (zh) | 粘合膜的制造方法和偏振片的制造方法 | |
| CN104422981B (zh) | 光学膜的制造方法 | |
| TW201610077A (zh) | 長條狀黏著薄膜之製造方法 | |
| WO2024058133A1 (ja) | コーティング層の除去方法及びコーティング層の除去装置 | |
| US20250026902A1 (en) | Coating film removing method and coating film removing equipment for removing coating film from coated film | |
| CN108292624A (zh) | 用于处理基材表面上的毫米-、微米-或纳米结构的方法 | |
| CN118251295A (zh) | 从带被膜的膜剥离被膜的方法及被膜的剥离装置 | |
| JP5284844B2 (ja) | ロール状金型を用いた光学シートの製造方法 | |
| WO2023189669A1 (ja) | コーティング層の除去方法及びコーティング層の除去装置 | |
| CN121057643A (zh) | 被膜剥离装置及被膜剥离方法 | |
| JPWO2023106002A5 (ja) | ||
| WO2023218811A1 (ja) | 被膜剥離方法および被膜剥離装置 | |
| JP2001179913A (ja) | 易接着性ポリエステルフィルム | |
| CN121240937A (zh) | 被膜剥离装置及被膜剥离方法 | |
| WO2026044237A1 (en) | Method and system for addressing buildup on printer cutting elements | |
| TWM679160U (zh) | 裁刀裝置 | |
| JP2009214513A (ja) | 離型性フィルムテープ・ロール及びその製造方法 | |
| KR20210001875A (ko) | 편광자의 제조 방법 및 편광자의 제조 장치 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| WWE | Wipo information: entry into national phase |
Ref document number: 2022574723 Country of ref document: JP |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 22903934 Country of ref document: EP Kind code of ref document: A1 |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 202280075943.3 Country of ref document: CN |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 12024551221 Country of ref document: PH |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 18713750 Country of ref document: US |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 11202403483P Country of ref document: SG |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2022903934 Country of ref document: EP |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 2022903934 Country of ref document: EP Effective date: 20240709 |