WO2024225455A1 - 方向性電磁鋼板 - Google Patents
方向性電磁鋼板 Download PDFInfo
- Publication number
- WO2024225455A1 WO2024225455A1 PCT/JP2024/016517 JP2024016517W WO2024225455A1 WO 2024225455 A1 WO2024225455 A1 WO 2024225455A1 JP 2024016517 W JP2024016517 W JP 2024016517W WO 2024225455 A1 WO2024225455 A1 WO 2024225455A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- width
- steel sheet
- grain
- linear
- oriented electrical
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images


Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F41/00—Apparatus or processes specially adapted for manufacturing or assembling magnets, inductances or transformers; Apparatus or processes specially adapted for manufacturing materials characterised by their magnetic properties
- H01F41/02—Apparatus or processes specially adapted for manufacturing or assembling magnets, inductances or transformers; Apparatus or processes specially adapted for manufacturing materials characterised by their magnetic properties for manufacturing cores, coils, or magnets
- H01F41/0206—Manufacturing of magnetic cores by mechanical means
- H01F41/0233—Manufacturing of magnetic circuits made from sheets
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/16—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys in the form of sheets
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D6/00—Heat treatment of ferrous alloys
- C21D6/008—Heat treatment of ferrous alloys containing Si
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1277—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties involving a particular surface treatment
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1294—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties involving a localised treatment
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/46—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for sheet metals
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/147—Alloys characterised by their composition
- H01F1/14766—Fe-Si based alloys
- H01F1/14775—Fe-Si based alloys in the form of sheets
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F27/00—Details of transformers or inductances, in general
- H01F27/24—Magnetic cores
- H01F27/245—Magnetic cores made from sheets, e.g. grain-oriented
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2201/00—Treatment for obtaining particular effects
- C21D2201/05—Grain orientation
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/02—Ferrous alloys, e.g. steel alloys containing silicon
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F27/00—Details of transformers or inductances, in general
- H01F27/34—Special means for preventing or reducing unwanted electric or magnetic effects, e.g. no-load losses, reactive currents, harmonics, oscillations, leakage fields
- H01F2027/348—Preventing eddy currents
Definitions
- the present invention relates to a grain-oriented electrical steel sheet. This application claims priority based on Japanese Patent Application No. 2023-073596, filed on April 27, 2023, the contents of which are incorporated herein by reference.
- Grain-oriented electrical steel sheets are soft magnetic materials and are primarily used as iron core materials for transformers, and therefore require magnetic properties such as high magnetization characteristics and low core loss.
- Iron loss is the power loss consumed as heat energy when an iron core is excited by an AC magnetic field, and from the perspective of energy conservation, it is desirable to have as low iron loss as possible.
- the level of iron loss is affected by factors such as magnetic susceptibility, sheet thickness, coating tension, amount of impurities, electrical resistivity, crystal grain size, and magnetic domain size.
- Patent Document 1 shows that it is possible to easily reduce iron loss in both the L direction and
- Patent Document 1 achieves a certain reduction in eddy current loss and thus a reduction in iron loss.
- the reduction in iron loss is not as great as expected from the division of the magnetic domain width, and there is room for improvement.
- laser irradiation of grain-oriented electrical steel sheet as proposed in Patent Document 1 is effective in reducing iron loss, there is a problem in that the closure domains formed by laser irradiation increase magnetostriction, thereby degrading noise characteristics.
- Patent Document 2 discloses a method for manufacturing grain-oriented electrical steel sheet with excellent magnetic properties, whose iron loss reduction effect does not disappear even after stress relief annealing. Patent Document 2 also shows that in a method for locally forming grooves in the final cold-rolled sheet, by making improvements to the shape of the grooves, it is possible to obtain even lower iron loss than in the past.
- Patent Document 2 is insufficient in reducing eddy current loss compared to the technology of imparting minute thermal distortion to steel sheets by irradiating them with laser light and plasma, and does not take noise characteristics into consideration.
- Patent Document 3 discloses a grain-oriented electrical steel sheet in which a plurality of strain regions extending in a direction transverse to the rolling direction are formed at periodic intervals s (mm) in the rolling direction, which are locally introduced into the surface layer of the steel sheet, and in which closure domain regions are formed in each of the strain regions, which are continuous over a width of 200 mm or more, and in which the width in the rolling direction at the steel sheet surface changes periodically, and in which each of the closure domain regions satisfies the following conditions: the ratio (Wmax/Wmin) of the maximum width Wmax in the rolling direction at the steel sheet surface to the minimum width Wmin is 1.2 to 2.2, the average width Wave in the rolling direction at the steel sheet surface is 80 ⁇ m to 250 ⁇ m, the maximum depth D in the sheet thickness direction is 32 ⁇ m or more, and (Wave x D)/s is 0.0007 mm to 0.0016 mm.
- Patent Document 3 describes that by periodically changing the width of the closure domain region in the rolling direction, it is possible to lower the magnetostrictive harmonic level and achieve both low iron loss and low noise.
- the width of the region where no strain is introduced changes, which inhibits the movement of the domain walls and increases hysteresis loss, and therefore the effect of reducing iron loss by subdividing the magnetic domain width cannot be fully obtained.
- the reason why Patent Document 1 does not achieve the effect of reducing iron loss as expected from the refinement of the magnetic domain width is believed to be because the movement of the magnetic domain walls is hindered and hysteresis loss increases.
- the present invention aims to provide a grain-oriented electrical steel sheet with lower core loss than conventional steel sheets.
- the inventors focused on the fact that in technology that achieves low iron loss and low noise by lowering the magnetostrictive harmonic level, although eddy current loss is reduced, hysteresis loss increases, and investigated methods for suppressing the increase in hysteresis loss and achieving even lower iron loss. As a result, they discovered that when introducing linear strain into the surface of a grain-oriented electrical steel sheet by laser irradiation or other means to refine magnetic domains, an increase in hysteresis loss can be suppressed by periodically increasing and decreasing the width of the introduced strain and by shifting the period of increase and decrease of the strain width between adjacent linear strains.
- a grain-oriented electrical steel sheet is a grain-oriented electrical steel sheet having a surface into which a plurality of linear strains extending in a direction at an angle of 60 to 120° to the longitudinal direction have been introduced, wherein the longitudinal spacing between adjacent ones of the linear strains is 2 to 10 mm, the width of the linear strains, which is the width in a direction perpendicular to the extension direction of the linear strain, increases and decreases periodically in the extension direction of the linear strain, with the period being 200 to 400 ⁇ m, the period of change in the width of adjacent ones of the plurality of linear strains is shifted by 0.4 to 0.6 periods in the extension direction of the linear strain, the ratio of the maximum width to the minimum width is 1.2 to 8.0, and the minimum width is 30 ⁇ m or more.
- FIG. 2 is a schematic diagram showing an example of a grain-oriented electrical steel sheet according to the present embodiment, in which linear strain is introduced into the surface. This is an example of a graph drawn using ImageJ, with DISTANCE on the horizontal axis and GRAY VALUE on the vertical axis.
- the grain-oriented electrical steel sheet 1 is a grain-oriented electrical steel sheet having a surface on which a plurality of linear distortions 2 extending in a direction of 60 to 120° with respect to the longitudinal direction (longitudinal direction of the grain-oriented electrical steel sheet) RD (which can also be said to be a direction of ⁇ 30° with respect to the width direction TD) have been introduced, and the spacing PL of adjacent plurality of linear distortions 2 in the longitudinal direction RD is 2 to 10 mm, and the width in the direction perpendicular to the extension direction of the linear distortions 2 is The width of the linear distortion 2 increases and decreases periodically in the extension direction of the linear distortion 2, with the period CYC being 200 to 400 ⁇ m.
- adjacent linear distortions 2, 2' have width change periods shifted by 0.4 to 0.6 periods in the extension direction of the linear distortion.
- the ratio (Tmax/Tmin) of the maximum width Tmax to the minimum width Tmin is 1.2 to 8.0, and the minimum width Tmin is 30 ⁇ m or more.
- the extension direction of the strain (corresponding to the scanning direction when strain is introduced by an energy ray such as a laser or an electron beam) is set at an angle of 60 to 120° with respect to the longitudinal direction (rolling direction). If the angle is out of this range, the 180° magnetic domain refinement effect of the steel sheet is reduced, and a sufficient iron loss reduction effect cannot be obtained.
- the distance between adjacent linear distortions in the longitudinal direction (normal rolling direction) RD exceeds 10 mm, the effect of refining the 180° magnetic domains is reduced, resulting in insufficient iron loss improvement. Therefore, the distance between adjacent linear distortions in the longitudinal direction is set to 10 mm or less. It is preferable that the distance between the linear distortions is approximately equal.
- the longitudinal interval between adjacent linear distortions is set to 2 mm or more.
- a linear distortion is a continuous distortion extending in one direction.
- the width of the linear distortion is intentionally increased or decreased as described below.
- the longitudinal distance PL between the multiple linear distortions is the distance from the center of a linear distortion to the center of an adjacent linear distortion.
- the width of the linear strain which is the width in the direction perpendicular to the extension direction of the linear strain, periodically increases and decreases in the extension direction of the linear strain.
- the introduced strain inhibits the movement of magnetic domain walls.
- Iron loss consists of eddy current loss and hysteresis loss, and the introduction of strain increases the hysteresis loss of iron loss.
- the present inventors discovered that by periodically increasing and decreasing the width of a single linear strain (the width in the direction perpendicular to the extension direction), a magnetic domain refinement effect can be obtained with a small amount of strain.
- the period of the change and the magnitude of the change must be within the range described below.
- "periodic" means that an error of about ⁇ 5% or less of the period is allowed (for example, ⁇ 10 ⁇ m is allowed for 200 ⁇ m, and ⁇ 20 ⁇ m is allowed for 400 ⁇ m).
- the period of change in width of the linear distortion is 200 to 400 ⁇ m>
- ⁇ The ratio of the maximum width to the minimum width of the linear distortion is 1.2 to 8.0>
- the width of part of the linear distortion is changed and part is made larger, thereby controlling the position at which the closure domains occur (controlling them so that they occur at the largest position) and controlling so that the period of the width change matches the domain width. If the ratio of the maximum width to the minimum width of the linear distortion (width ratio) is less than 1.2, the result will be the same as in the conventional case (when a distortion of uniform width is introduced), and there is a concern that the closure domains will occur in unintended positions, and sufficient magnetic domain refinement effect will not be obtained.
- the width ratio is set to 1.2 to 8.0.
- the maximum width it is preferable that when an isosceles triangle is drawn with the length of one period (the length from one valley to the next valley when the width profile is illustrated) as its base and the position where the linear distortion is at its maximum width as its apex, the base angle of the triangle is 45° or less.
- the width of the linear distortion is set to 30 ⁇ m or more even at the smallest portion (narrowest portion).
- the cycle of the width change corresponds to the final magnetic domain width. If the cycle of the change exceeds 400 ⁇ m, the magnetic domain width is wide and a sufficient effect of improving iron loss cannot be obtained. Furthermore, although shortening the period reduces the magnetic domain width, if the period is too short, the magnetic domain width will correspond to multiple periods (for example, even if the period is 150 ⁇ m, the magnetic domain width will be twice that, or 300 ⁇ m), and there is a concern that the magnetic domain width will instead become wider. Therefore, the period of the width change is set to 200 ⁇ m or more.
- adjacent linear distortions have width change periods shifted by 0.4 to 0.6 periods in a direction perpendicular to the extension direction of the linear distortions>
- the width of the introduced strain is changed periodically to obtain the same magnetic domain width as one period of the strain.
- the periodic change in the width of the linear distortion causes the width of the non-distorted area to vary depending on the position when viewed in the longitudinal direction of the grain-oriented electrical steel sheet, making it difficult for the domain walls to move.
- the width of the region where no strain is introduced is made substantially constant by shifting the period of the change in width of adjacent linear strains among the multiple linear strains.
- the shift in period is about half a period (0.5 period) as shown in Fig. 1, and a shift of 0.4 to 0.6 period is acceptable.
- the amount of shift is evaluated by using the direction perpendicular to the extension direction of the linear strain as a reference and the amount of shift in the extension direction as a unit of period.
- the location where the linear strain is introduced into the grain-oriented electrical steel sheet can be identified by the following method. That is, where distortion has been applied to the steel plate, the distortion causes distortion in the iron crystal lattice.
- a method called X-ray topography is used to detect this distortion.
- An overview of this method is given below. Normally, when X-rays are incident on a crystal lattice, the X-rays are reflected at specific angles of incidence and reflection according to each crystal lattice plane, and in this case the angles of incidence and reflection are equal. This is called the Bragg diffraction condition, and depending on the distortion of the crystal, i.e. the magnitude of the distortion of the iron crystal in this patent, the reflection angle changes slightly relative to the angle of incidence or the reflection intensity is weakened.
- the X-ray topography device used was a Rigaku XRTmicron
- the X-ray source was a Cu target
- the diffraction plane during imaging was iron (310).
- the CCD resolution was 2.4 ⁇ m
- the digital resolution was 16 bits.
- the procedure is as follows: first, a grain-oriented electrical steel sheet in which strain has been imparted by energy rays is processed by cutting 100 mm in the rolling direction and 100 mm in the sheet width direction to prepare a sample. If processing strain is imparted to the steel sheet during processing, it must be done carefully because it affects the X-ray reflection behavior.
- an insulating coating is applied to the surface of a normal grain-oriented electrical steel sheet, but whether or not it is applied, the location of the strain can be identified, so it is important to prepare the sample so that as little processing strain as possible is imparted according to the state of the original sample.
- a topography image is photographed in the sheet width direction using Snap Shot in high resolution mode.
- the field of view diameter during photography is 6 to 7 mm in the sheet width direction and 7 to 8 mm in the rolling direction.
- a TDI (Time Delay Integration) scan may be performed in advance.
- the locations where distortion has been applied are specifically identified from the captured topography image using image analysis software called ImageJ.
- a topography image is developed on ImageJ, and an ROI (Range of Interest) is set as an analysis range (pixel width and height are 2.406 ⁇ m).
- the ROI is rectangular, and its range is 646 pixels (equivalent to approximately 1.55 mm) in the rolling direction and 84 pixels (equivalent to approximately 0.20 mm) in the plate width direction.
- the side parallel to the rolling direction is referred to as the ROI long side
- the side parallel to the plate width direction is referred to as the ROI short side.
- the ROI is set so that the portion to which the strain is applied fits within the rectangle. At this time, it may be visually observed, so the portion to which the strain is applied is set to be located at the center of the ROI long side.
- a graph is drawn in the ROI setting range with the horizontal axis set to DISTANCE and the vertical axis set to GRAY VALUE.
- the graph drawing function is part of the functions of ImageJ and is used.
- a spectrum having a negative peak as shown in FIG. 2 is obtained.
- the Gray Scale is read for the plateau-shaped portions at both ends of the spectrum, and their average value is calculated.
- this average value is called I Ave.
- the negative peak intensity (minimum value of the spectrum) in the spectrum is called I Bottom .
- the difference between I Ave. and I Bottom is defined as ⁇ I Height .
- I HH Half Height
- I HH is the Gray Scale value equivalent to half the peak intensity.
- the width W of the portion where the distortion is applied is defined as the DISTANCE between two points corresponding to I HH .
- IHH IHeight + (0.5 ⁇ IHeight )...(1)
- the grain-oriented electrical steel sheet according to the present embodiment can obtain the above-mentioned effects regardless of the manufacturing method, however, the manufacturing method including the following configuration is preferable because it can be manufactured relatively stably.
- An irradiation step in which an energy beam is irradiated onto a surface of a grain-oriented electrical steel sheet obtained by a known method at approximately constant intervals of 2 to 10 mm in the longitudinal direction, by scanning the energy beam in a direction of 60 to 120° with respect to the longitudinal direction while periodically changing the width (thickness) of the energy beam in the direction perpendicular to the scanning direction, thereby introducing a plurality of linear strains into the grain-oriented electrical steel sheet.
- the grain-oriented electrical steel sheet to be irradiated with the energy rays may be a steel sheet obtained by a known method, for example, a grain-oriented electrical steel sheet that satisfies JIS C2553:2019. It is preferable that the grain-oriented electrical steel sheet has a magnetic flux density B8 (magnetic flux density at 800 A/m) of 1.90 T or more, and more preferable that the grain-oriented electrical steel sheet has a B8 of 1.92 T or more.
- B8 magnetic flux density at 800 A/m
- the energy beam is irradiated by scanning the energy beam in a direction of 60 to 120° to the longitudinal direction at approximately constant intervals of 2 to 10 mm in the longitudinal direction (rolling direction) to introduce a plurality of linear strains extending in a direction of 60 to 120° to the longitudinal direction.
- the energy beam is preferably a continuous wave laser to obtain a linear distortion that is continuous in the extension direction.
- a continuous wave laser is preferably used.
- the laser irradiation conditions may be any known conditions as long as they are within a range in which strain can be introduced into the surface of the grain-oriented electrical steel sheet.
- the width of the energy line in the direction perpendicular to the scanning direction can be changed periodically by installing a shutter whose width varies periodically in the scanning direction immediately after the lens. Furthermore, by changing the position of the shutter during scanning, when the periods of adjacent linear distortions are shifted within a given range, the periods of the width changes can be shifted.
- a grain-oriented electrical steel sheet having a Si content of 3.25% and a thickness of 0.23 mm was prepared.
- the grain-oriented electrical steel sheet had a magnetic flux density B8 of 1.93 T and an iron loss W17/50 of 0.90 W/kg.
- This grain-oriented electrical steel sheet was irradiated by scanning a continuous wave laser in the longitudinal direction (rolling direction) at a constant interval (pitch) shown in Table 1, in the direction (angle relative to the longitudinal direction) shown in Table 1.
- a polygon mirror was used for scanning, and a shutter with a width that periodically varies in the scanning direction was installed immediately after the lens, thereby changing the width of the distortion in the period shown in Table 1.
- the shift in period of the change in the width of the strain between adjacent linear strains was as shown in Table 1.
- the magnetic properties of the obtained grain-oriented electrical steel sheets were evaluated in the following manner.
- Magnetic property evaluation A sample having a width of 60 mm and a length of 300 mm was taken, including the center position of the sheet width of the grain-oriented electrical steel sheet of each test number. The length direction of the sample was parallel to the rolling direction. Using this sample, the magnetic flux density was determined by a single sheet magnetic property test (SST test) in accordance with JIS C 2556 (2015). Specifically, a magnetic field of 800 A/m was applied to the sample to determine the magnetic flux density B8 (T). Furthermore, using the above sample, the iron loss W17/50 (W/kg) was measured when the frequency was 50 Hz and the maximum magnetic flux density was 1.7 T in accordance with JIS C 2556 (2015).
- this invention by realizing magnetic domain refinement that does not impede the movement of magnetic domain walls, it is possible to suppress an increase in hysteresis loss while reducing eddy current loss, resulting in a grain-oriented electrical steel sheet with low iron loss. Therefore, this invention has a high industrial applicability.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Physics & Mathematics (AREA)
- Power Engineering (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Crystallography & Structural Chemistry (AREA)
- Thermal Sciences (AREA)
- Manufacturing & Machinery (AREA)
- Electromagnetism (AREA)
- Dispersion Chemistry (AREA)
- Manufacturing Of Steel Electrode Plates (AREA)
- Soft Magnetic Materials (AREA)
Abstract
Description
本願は、2023年04月27日に、日本に出願された特願2023-073596号に基づき優先権を主張し、その内容をここに援用する。
鉄損とは、鉄心を交流磁場で励磁した場合に、熱エネルギーとして消費される電力損失であり、省エネルギーの観点から、鉄損はできるだけ低いことが求められる。鉄損の高低には、磁化率、板厚、被膜張力、不純物量、電気抵抗率、結晶粒径、磁区サイズなどが影響する。方向性電磁鋼板に関し、様々な技術が開発されている現在においても、エネルギー効率を高めるため、鉄損を低減する研究開発が継続されている。
低鉄損化する方法の一つとして、鋼板表面にレーザ照射を行う技術が提案されている。この技術では、レーザ照射により表面に歪が導入され、180°磁区幅が細分化されることで鉄損の一部である渦電流損を低減することができるとされている。
特許文献1では、容易に、かつ高い生産性を確保しながら、方向性電磁鋼板のL方向及びC方向の両方向における鉄損を低減することができることが示されている。
また、特許文献1に提案されるような方向性電磁鋼板へのレーザ照射は、鉄損の低減には効果的であるものの、レーザ照射によって形成される還流磁区が、磁歪を大きくすることで騒音特性が劣化するという課題があった。
しかしながら、本発明者らが検討した結果、特許文献3の技術では、歪が導入されていない領域の幅が変化することで、磁壁の移動が阻害され、ヒステリシス損が増加するので、磁区幅の細分化による鉄損低減効果が十分に得られない。
また、特許文献1で、磁区幅の細分化から予想されるほどの鉄損の低減効果が得られないのも、磁壁の移動が阻害され、ヒステリシス損が増加しているからであると考えられる。
その結果、方向性電磁鋼板の表面にレーザ照射等によって線状の歪を導入して磁区細分化を行う際に、導入する歪の幅を周期的に増減させるとともに、隣り合う線状の歪同士で、歪の幅の増減の周期をずらすことで、ヒステリシス損の増加を抑えることができるとの知見を得た。
[1]本発明の一態様に係る方向性電磁鋼板は、表面に、長手方向に対して60~120°の方向に延在する複数の線状の歪が導入された方向性電磁鋼板であって、隣り合う前記複数の線状の歪の、前記長手方向の間隔が、それぞれ2~10mmであり、前記線状の歪の延在方向に垂直な方向の幅である前記線状の歪の幅が、前記線状の歪の前記延在方向において周期的に増減しており、周期が、200~400μmであり、前記複数の線状の歪のうち、隣り合う線状の歪は、前記幅の変化の前記周期が、前記線状の歪の前記延在方向に0.4~0.6周期分ずれており、前記幅の最小に対する前記幅の最大の比が、1.2~8.0であり、前記幅の最小は、30μm以上である。
図1に示すように、本実施形態に係る方向性電磁鋼板1は、表面に、長手方向(方向性電磁鋼板の長手方向)RDに対して60~120°の方向(幅方向TDに対して±30°の方向とも言える)に延在する複数の線状の歪2が導入された、方向性電磁鋼板であって、隣り合う複数の線状の歪2の、長手方向RDの間隔PLが、それぞれ2~10mmであり、線状の歪2の延在方向に垂直な方向の幅である線状の歪2の幅が、線状の歪2の延在方向において周期的に増減しており、周期CYCが、200~400μmであり、複数の線状の歪2のうち、隣り合う線状の歪2,2’は、幅の変化の周期が、線状の歪の延在方向に0.4~0.6周期分ずれており、幅の最小Tminに対する幅の最大Tmaxの比(Tmax/Tmin)が、1.2~8.0であり、前記幅の最小Tminが30μm以上である。
以下、それぞれの限定理由について説明する。
<隣り合う複数の線状の歪の、長手方向の間隔が、それぞれ2~10mm>
方向性電磁鋼板では、長手方向(製造工程における圧延方向)RDに磁化容易軸が揃っており、長手方向に垂直方向に近い方向にレーザや電子ビーム等のエネルギー線を走査しながら照射して方向性電磁鋼板の表面に歪を導入すると、180°磁区細分化作用によって、鉄損が更に低減される。
本実施形態において、歪の延在方向(レーザや電子ビーム等のエネルギー線によって歪を導入する場合には、その走査方向に相当)を長手方向(圧延方向)に対して60~120°の角度とする。角度がこの範囲から外れると、鋼板の180°磁区細分化作用は少なくなり十分な鉄損低減効果が得られない。
また、隣り合う複数の線状の歪の、長手方向(通常圧延方向)RDの間隔が10mm超であると、180°磁区の磁区細分化効果が減少するため鉄損改善効果が不足する。そのため、それぞれの隣り合う線状の歪の、長手方向の間隔は、10mm以下とする。複数の線状の歪の間隔は、略等間隔であることが好ましい。
一方、照射間隔を小さくすると基本的には鉄損が小さくなるものの、過度に小さくなると磁区細分化効果が飽和し渦電流損がほとんど低下しなくなる一方で、歪によるヒステリシス損の増加が顕著になり、鉄損が悪化する。また、騒音特性が劣化する場合がある。そのため、それぞれの隣り合う線状の歪の、長手方向の間隔は、2mm以上とする。
線状の歪とは、一方向に延在する連続的な歪である。本実施形態では、後述するようにその幅を意図的に増減させる。
ここで、本実施形態において、複数の線状の歪の長手方向の間隔PLとは、線状の歪の中心から隣り合う線状の歪の中心までの間隔である。
上述のように、方向性電磁鋼板の表面エネルギー線を照射して線状の歪を導入することによって、渦電流損を低下させることができる。一方で、導入された歪は磁壁の移動を阻害する。鉄損は、渦電流損とヒステリシス損からなるが、歪の導入により、鉄損のうちヒステリシス損が増加する。
ヒステリシス損を増加させないためには、歪の量を小さくすることが好ましいが、一方で、歪の量が小さいと、磁区細分化効果が小さくなる。
本発明者らは、1本の線状の歪において、歪の幅(延在方向に垂直な方向の幅)を周期的増減させることで、少量の歪で磁区細分化効果を得られることを見出した。
ただし、その変化の周期や、変化の大きさについては、十分な効果を得るため、後述する範囲とする必要がある。
ここで本実施形態において周期的にとは、周期のおよそ±5%以下の誤差は許容する(例えば200μmの場合±10μm、400μmの場合±20μmは許容する)。
<線状の歪の幅の最小に対する幅の最大の比が、1.2~8.0である>
本実施形態に係る方向性電磁鋼板では、線状の歪の一部の幅を変化させ、一部を大きくすることで、還流磁区の発生位置を制御し(最も大きい位置から発生するように制御し)、幅の変化の周期と磁区幅とが一致するように制御している。
線状の歪の幅の最小に対する幅の最大の比(幅の比)が1.2未満では、従来(均一な幅の歪を導入した場合)と同様であり、還流磁区の発生位置が意図しない位置となり、十分な磁区細分化効果が得られないことが懸念される。
一方、幅の比が8.0超であっても、還流磁区の発生位置が意図しない位置となり、十分な磁区細分化効果が得られないことが懸念される。そのため、幅の比を1.2~8.0とする。
幅の最大値に関し、好ましくは、1周期の長さ(幅のプロフィールを図示した際の谷から隣の谷までの長さ)を底辺、線状の歪の最大幅となる位置を頂点とする二等辺三角形を描いた際に、その三角形の底角が45°以下であることが好ましい。
磁区細分化効果を十分に得るため、線状の歪の幅は、最小の部分(最も細い部分)でも30μm以上とする。
また、幅の変化の周期は、最終的に得られる磁区幅に相当する。変化の周期が400μm超では、磁区幅が広く、十分な効果が鉄損の改善効果が得られない。
また、周期を短くすることで、磁区幅が小さくなるものの、周期が短くなりすぎると、磁区幅が、複数周期分に対応するようになり(例えば周期が150μmであっても、磁区幅はその2倍の300μmとなり)、むしろ、磁区幅が広くなることが懸念される。そのため、幅の変化の周期は200μm以上とする。
上述の通り、導入される歪の幅を周期的に変化させ、歪の1周期と同じ磁区幅を得る。しかしながら、複数の線状の歪を導入するに際し、一様に線状の歪を導入する場合、磁壁が動きにくくなり、磁区幅の細分化による鉄損低減効果が十分に得られない。
これは、線状の歪の幅の周期的な変化によって、方向性電磁鋼板の長手方向で見た際に、歪の導入されてない領域の幅が位置によって異なることで、磁壁が動きにくくなることが理由であると考えられる。
そのため、本実施形態に係る方向性電磁鋼板では、複数の線状の歪のうち、隣り合う線状の歪は、前記幅の変化の周期を、ずらすことで歪が導入されていない領域の幅を略一定にする。周期のずれは、図1に示すように、約半周期(0.5周期)であり、0.4~0.6周期であれば許容される。ずれの量は、線状の歪の延在方向に垂直な方向を基準として、延在方向のずれ量を、周期を単位として、評価する。
すなわち鋼板で歪が付与された箇所は、歪により鉄の結晶格子に歪みが生じる。この歪みを検出する方法として、X線トポグラフィという方法を用いる。以下にその概要を説明する。通常結晶格子にX線を入射した場合、各結晶格子面に応じた特定の入射角度と反射角度にてX線の反射が生じ、その場合入射角度と反射角度は等しくなる。これはブラッグ回折条件と呼ばれるが、結晶の歪み、すなわち本特許の場合は鉄結晶の歪みの大きさにより、入射角度に対して反射角度がわずかに変化したり反射強度が弱められる。この現象を利用する分析法である。
分析に際し、X線トポグラフィ装置は、リガク製のXRTmicronを用い、X線源はCuターゲットとする。また撮影時の回折面は鉄の(310)とする。CCD解像度を2.4μm、Digital分解能を16bitとする。
手順としては、まずエネルギー線により鋼板に歪が付与された方向性電磁鋼板について圧延方向に100mm、板幅方向に100mmを切断等により加工し試料を準備する。加工の際に加工歪が鋼板に付与されると、それがX線反射挙動に影響するので注意深く行う必要がある。得た試料について、通常の方向性電磁鋼板にはその表面に絶縁被膜が施されているが、それが施されていてもいなくても、いずれでも歪の付与箇所を特定できるので元の試料の状態に応じてなるべく加工歪が付与されないように準備することが肝要である。そして、板幅方向に対して、トポグラフィ画像を高解像モードでのSnap Shot撮影とする。撮影時の視野径は、板幅方向6~7mm、圧延方向7~8mmとする。撮影箇所を決めるために、事前にTDI(Time Delay Integration)スキャンを実施しても良い。
次に撮影されたトポグラフィ画像から、ImageJという画像解析ソフトを用いて、歪が付与された箇所を具体的に特定する。
特定に際しては、ImageJ上で、トポグラフィ画像を展開し、解析範囲であるROI(Range of Interest)を設定する(ピクセル幅および高さは2.406μm)ROIは矩形であり、その範囲は圧延方向を646ピクセル(およそ1.55mm相当)とし、板幅方向を84ピクセル(およそ0.20mm相当)とする。以降、圧延方向に対して平行な辺をROI長辺、板幅方向に対して平行な辺をROI短辺と呼称する。矩形内に歪が付与された箇所が収まるようにROIを設定する。この時、目視でも良いので、歪が付与された箇所がROI長辺の中心に位置するように設定する。ROI設定が終わったら、次はROI設定範囲において、横軸をDISTANCE、縦軸をGRAY VALUEとして、グラフを描画する。グラフ描写機能はImageJの機能の一部でありこれを用いる。これにより、図2に示す様な、負のピークを有するスペクトルが得られる。スペクトル両端のプラトー形状部分についてGray Scaleを読み取り、それらの平均値を算出する。以降、この平均値をIAve.と呼ぶ。スペクトルにおける、負のピーク強度(スペクトルの最小値)をIBottomとする。IAve.とIBottomの差分を、ΔIHeightと定義する。ここで、以下の式で定義できる、IHH(Half Height)という概念を導入する。IHHとは、ピーク強度の半分に相当するGray Scale値である。歪が付与された箇所の幅Wを、IHHに対応する2点間のDISTANCEと定義する。
IHH = IHeight+(0.5×IHeight)・・・(1)
本実施形態に係る方向性電磁鋼板は、製造方法によらず、上記の特徴を有していればその効果が得られる。しかしながら、以下の構成を含む製造方法によれば比較的安定して製造できるので、好ましい。
(1)公知の方法で得られた方向性電磁鋼板の表面に、長手方向に2~10mmの略一定の間隔で、エネルギー線を、走査方向に垂直な方向のエネルギー線の幅(太さ)を周期的に変化させながら、前記長手方向に対して60~120°の方向に走査することで照射して、方向性電磁鋼板に複数の線状の歪を導入する照射工程。
エネルギー線は、延在方向に連続した線状の歪を得るため、連続波レーザであることが好ましい。また、電子ビームやパルス波の場合板幅方向の歪が生じやすいので、連続波である連続波レーザであることが好ましい。
レーザの照射条件は、方向性電磁鋼板の表面に歪を導入できる範囲であれば公知の条件を採用することができる。
また走査する際に、シャッターの位置を変化させることで、隣り合う線状の歪において任意の範囲で周期をずらす場合、幅の変化の周期をずらすことができる。
この方向性電磁鋼板に対し、長手方向(圧延方向)に表1に示す一定の間隔(ピッチ)で、表1に示す方向(長手方向に対する角度)に、連続波レーザを走査して照射した。走査に際しては、ポリゴンミラーにより走査するとともに、レンズの直後に走査方向に周期的に幅が異なるシャッターを設置することで、表1の周期で歪の幅を変化させた。
隣り合う線状の歪における歪の幅の変化の周期のずれは、表1に示す通りとした。
得られた方向性電磁鋼板に対し、以下の要領で、磁気特性を評価した。
各試験番号の方向性電磁鋼板の板幅中央位置を含む、幅60mm×長さ300mmのサンプルを採取した。サンプルの長さ方向は、圧延方向に平行であった。このサンプルを用いて、JIS C 2556(2015)に準拠して、単板磁気特性試験(SST試験)により、磁束密度を求めた。具体的には、サンプルに800A/mの磁場を付与して、磁束密度B8(T)を求めた。
さらに、上記サンプルを用いて、JIS C 2556(2015)に準拠して、周波数を50Hz、最大磁束密度を1.7Tとしたときの鉄損W17/50(W/kg)を測定した。
また、最大磁束密度を1.7Tとしたときのヒステリシスループを測定し、そこから得られたヒステリシス損とW17/50から渦電流損を求めた。
結果を表2に示す。

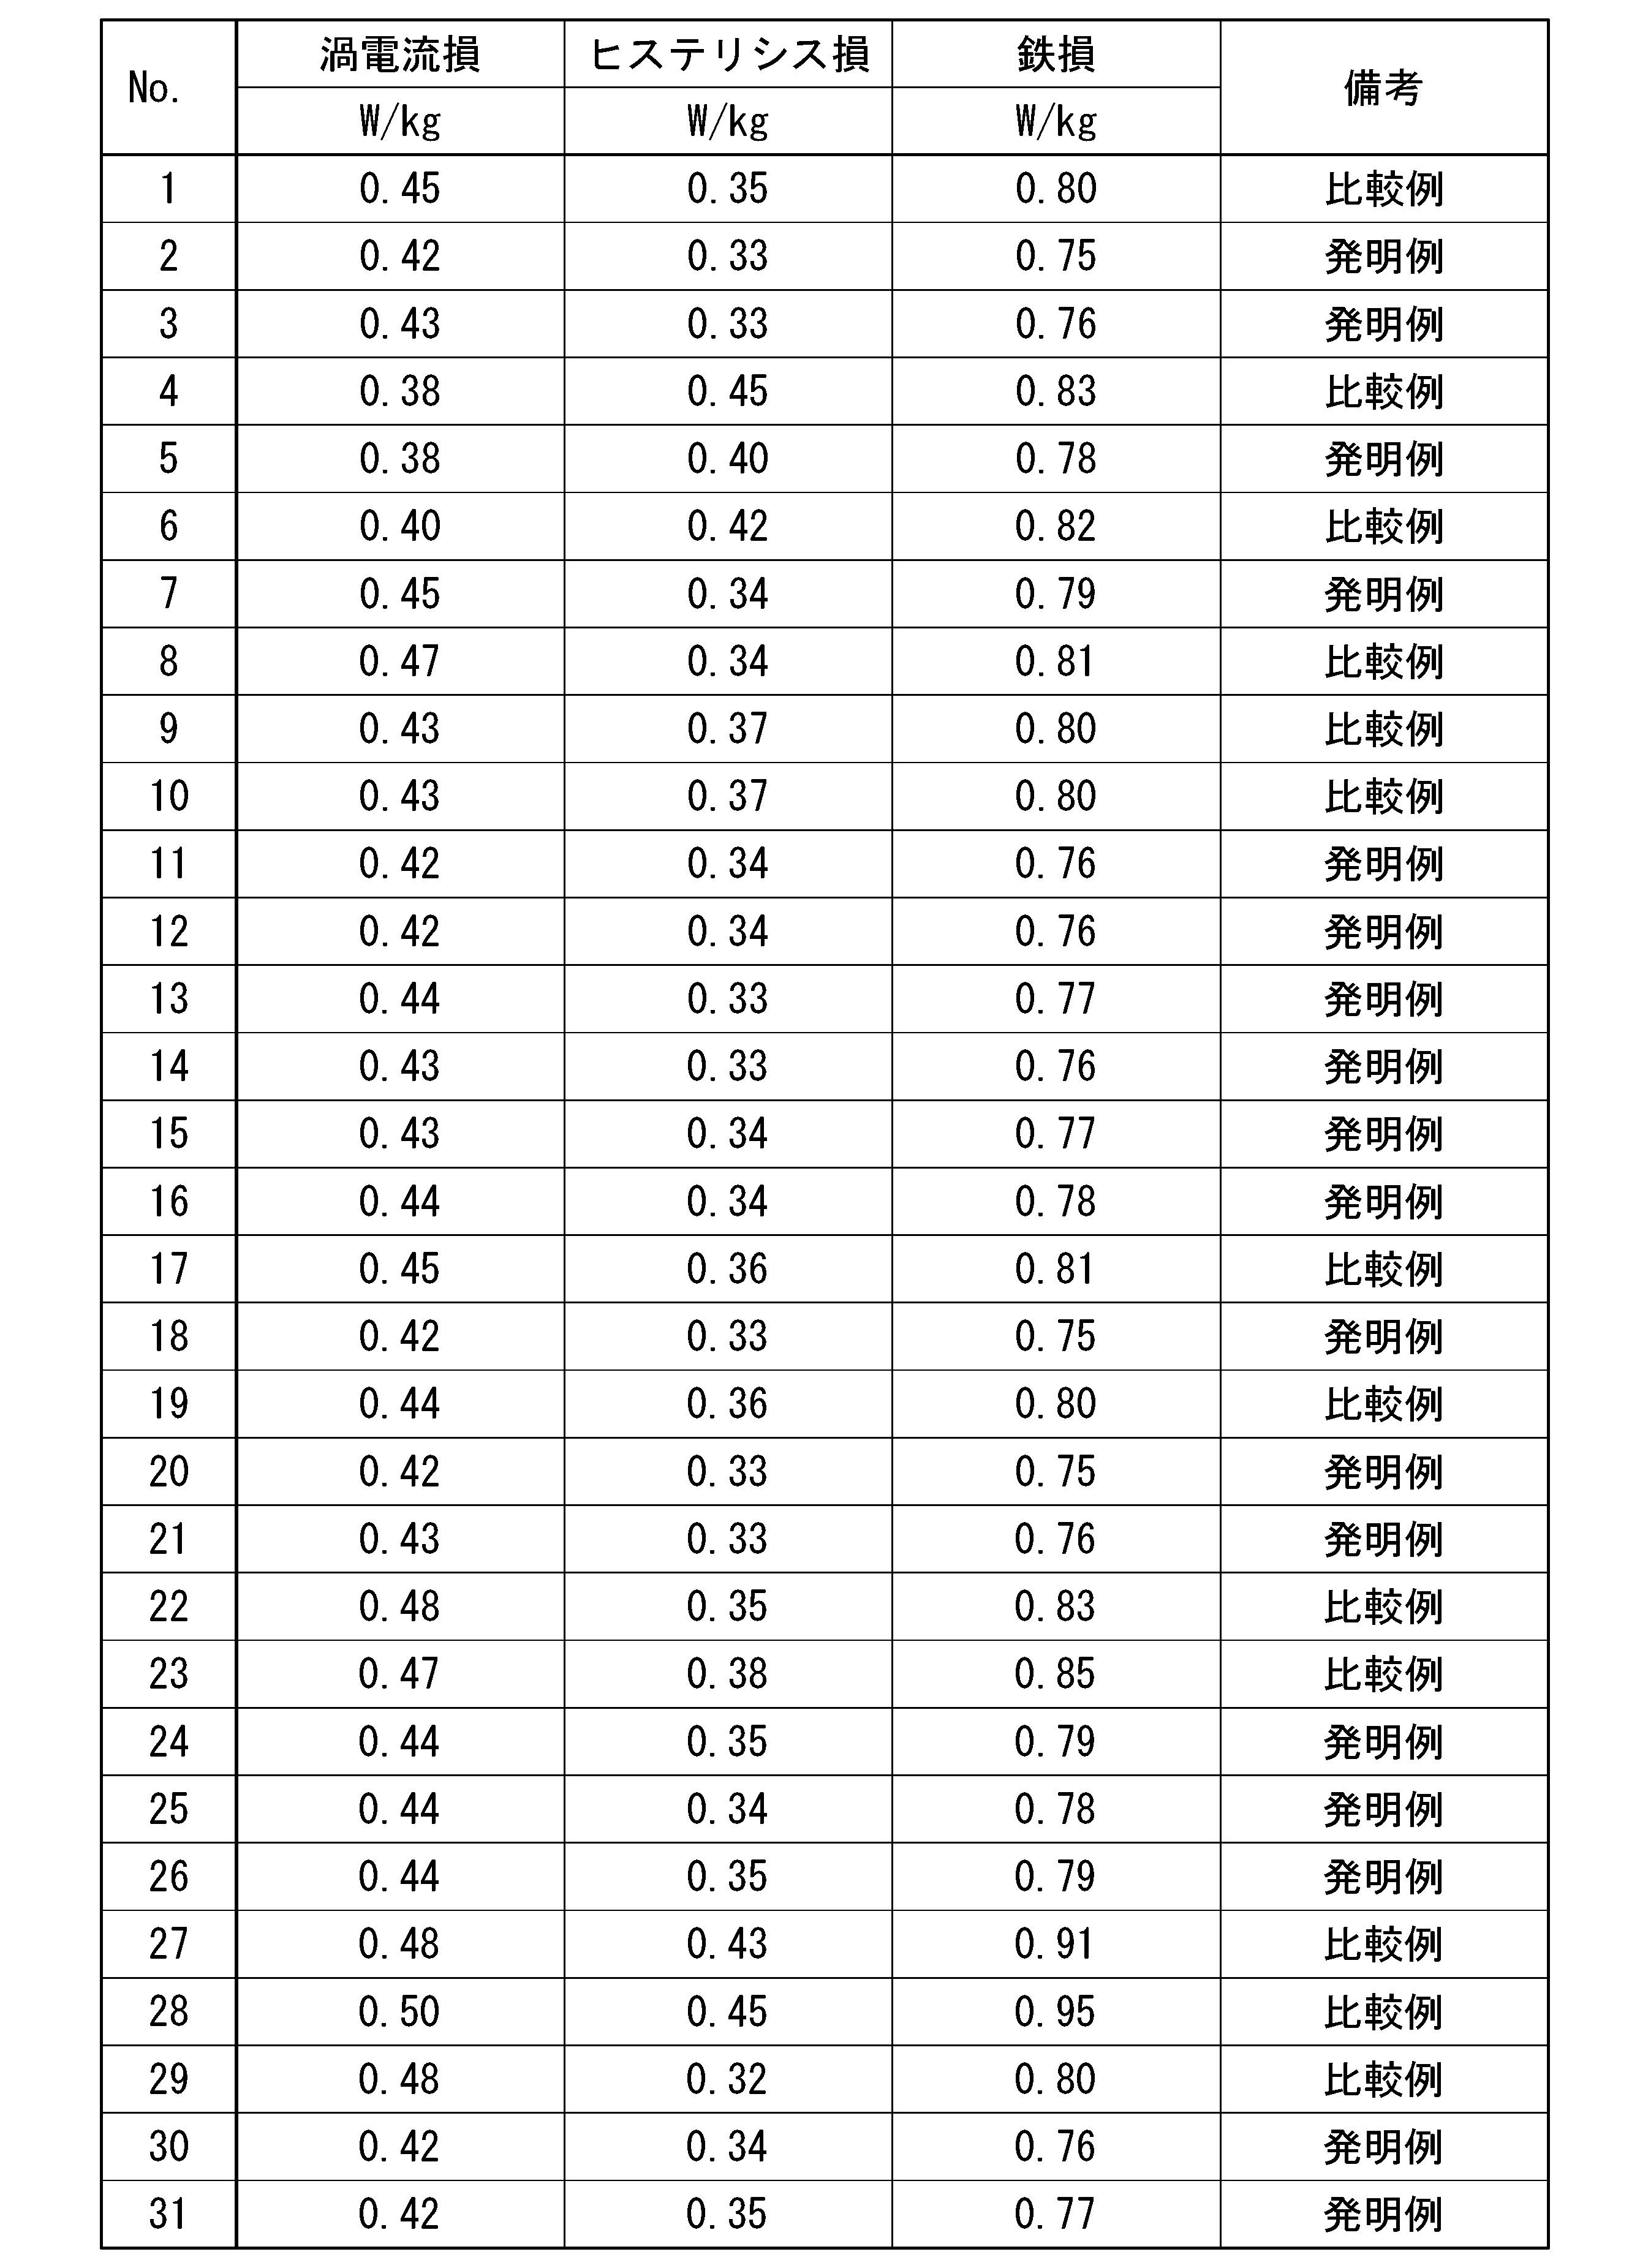
これに対し、比較例であるNo.1、4、6、8~10、17、19、22、23、27~29では、線状の歪の幅の変化の周期、歪の最大幅/最小幅、歪の幅の最小、周期のずれ、複数の線状の歪の間隔、延在方向の少なくとも1つが本発明範囲外であり、鉄損が大きかった。
2 線状の歪
2’ 2と隣り合う線状の歪
RD 鋼板(方向性電磁鋼板)の長手方向
TD 鋼板(方向性電磁鋼板)の幅方向
PL 線状の歪の、鋼板(方向性電磁鋼板)の長手方向の間隔
CYC 周期
Tmin 幅の最小
Tmax 幅の最大
Claims (1)
- 表面に、長手方向に対して60~120°の方向に延在する複数の線状の歪が導入された方向性電磁鋼板であって、
隣り合う前記複数の線状の歪の、前記長手方向の間隔が、それぞれ2~10mmであり、
前記線状の歪の延在方向に垂直な方向の幅である前記線状の歪の幅が、前記線状の歪の前記延在方向において周期的に増減しており、周期が、200~400μmであり、
前記複数の線状の歪のうち、隣り合う線状の歪は、前記幅の変化の前記周期が、前記線状の歪の前記延在方向に0.4~0.6周期分ずれており、
前記幅の最小に対する前記幅の最大の比が、1.2~8.0であり、
前記幅の最小は、30μm以上である、
方向性電磁鋼板。
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP24797198.9A EP4703490A1 (en) | 2023-04-27 | 2024-04-26 | Grain-oriented electrical steel sheet |
| CN202480026803.6A CN120981595A (zh) | 2023-04-27 | 2024-04-26 | 方向性电磁钢板 |
| JP2024551524A JP7620258B1 (ja) | 2023-04-27 | 2024-04-26 | 方向性電磁鋼板 |
| KR1020257034995A KR20250168406A (ko) | 2023-04-27 | 2024-04-26 | 방향성 전자 강판 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2023073596 | 2023-04-27 | ||
| JP2023-073596 | 2023-04-27 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2024225455A1 true WO2024225455A1 (ja) | 2024-10-31 |
Family
ID=93256872
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2024/016517 Ceased WO2024225455A1 (ja) | 2023-04-27 | 2024-04-26 | 方向性電磁鋼板 |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP4703490A1 (ja) |
| JP (1) | JP7620258B1 (ja) |
| KR (1) | KR20250168406A (ja) |
| CN (1) | CN120981595A (ja) |
| WO (1) | WO2024225455A1 (ja) |
Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5296051A (en) * | 1993-02-11 | 1994-03-22 | Kawasaki Steel Corporation | Method of producing low iron loss grain-oriented silicon steel sheet having low-noise and superior shape characteristics |
| JPH06299244A (ja) | 1993-04-12 | 1994-10-25 | Kawasaki Steel Corp | 磁気特性に優れた電磁鋼板の製造方法 |
| JP2007277644A (ja) * | 2006-04-07 | 2007-10-25 | Nippon Steel Corp | 磁気特性の優れた方向性電磁鋼板の製造方法 |
| JP4669565B2 (ja) | 2007-12-12 | 2011-04-13 | 新日本製鐵株式会社 | レーザ光の照射により磁区が制御された方向性電磁鋼板の製造方法 |
| JP2013159846A (ja) * | 2012-02-08 | 2013-08-19 | Jfe Steel Corp | 方向性電磁鋼板 |
| WO2016136176A1 (ja) * | 2015-02-24 | 2016-09-01 | Jfeスチール株式会社 | 方向性電磁鋼板及びその製造方法 |
| JP2023073596A (ja) | 2021-11-16 | 2023-05-26 | 日本電信電話株式会社 | 異常発生箇所判定装置、異常発生箇所判定方法及びプログラム |
-
2024
- 2024-04-26 KR KR1020257034995A patent/KR20250168406A/ko active Pending
- 2024-04-26 EP EP24797198.9A patent/EP4703490A1/en active Pending
- 2024-04-26 JP JP2024551524A patent/JP7620258B1/ja active Active
- 2024-04-26 CN CN202480026803.6A patent/CN120981595A/zh active Pending
- 2024-04-26 WO PCT/JP2024/016517 patent/WO2024225455A1/ja not_active Ceased
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5296051A (en) * | 1993-02-11 | 1994-03-22 | Kawasaki Steel Corporation | Method of producing low iron loss grain-oriented silicon steel sheet having low-noise and superior shape characteristics |
| JPH06299244A (ja) | 1993-04-12 | 1994-10-25 | Kawasaki Steel Corp | 磁気特性に優れた電磁鋼板の製造方法 |
| JP2007277644A (ja) * | 2006-04-07 | 2007-10-25 | Nippon Steel Corp | 磁気特性の優れた方向性電磁鋼板の製造方法 |
| JP4669565B2 (ja) | 2007-12-12 | 2011-04-13 | 新日本製鐵株式会社 | レーザ光の照射により磁区が制御された方向性電磁鋼板の製造方法 |
| JP2013159846A (ja) * | 2012-02-08 | 2013-08-19 | Jfe Steel Corp | 方向性電磁鋼板 |
| WO2016136176A1 (ja) * | 2015-02-24 | 2016-09-01 | Jfeスチール株式会社 | 方向性電磁鋼板及びその製造方法 |
| JP6060988B2 (ja) | 2015-02-24 | 2017-01-18 | Jfeスチール株式会社 | 方向性電磁鋼板及びその製造方法 |
| JP2023073596A (ja) | 2021-11-16 | 2023-05-26 | 日本電信電話株式会社 | 異常発生箇所判定装置、異常発生箇所判定方法及びプログラム |
Non-Patent Citations (1)
| Title |
|---|
| See also references of EP4703490A1 |
Also Published As
| Publication number | Publication date |
|---|---|
| JP7620258B1 (ja) | 2025-01-23 |
| JPWO2024225455A1 (ja) | 2024-10-31 |
| KR20250168406A (ko) | 2025-12-02 |
| EP4703490A1 (en) | 2026-03-04 |
| CN120981595A (zh) | 2025-11-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP4669565B2 (ja) | レーザ光の照射により磁区が制御された方向性電磁鋼板の製造方法 | |
| US8034196B2 (en) | Low core loss grain-oriented electrical steel plate and method of manufacturing the same | |
| KR102639341B1 (ko) | 방향성 전기강판 및 그 제조 방법 | |
| KR102857829B1 (ko) | 방향성 전자 강판 및 그 제조 방법 | |
| JP7678365B2 (ja) | 方向性電磁鋼板及びその製造方法 | |
| EP3409796B1 (en) | Grain-oriented electrical steel sheet and method for manufacturing same | |
| JP7620258B1 (ja) | 方向性電磁鋼板 | |
| JP2021169655A (ja) | 方向性電磁鋼板、方向性電磁鋼板の磁区構造の解析方法及び解析システム | |
| KR102871723B1 (ko) | 방향성 전자 강판 및 그 제조 방법 | |
| EP4317468A1 (en) | Grain-oriented electromagnetic steel sheet and method for producing same | |
| US20230395301A1 (en) | Wound core | |
| JP2006117964A (ja) | 磁気特性の優れた方向性電磁鋼板とその製造方法 | |
| EP4707420A1 (en) | Grain-oriented electromagnetic steel sheet and magnetic domain control method | |
| RU2819013C2 (ru) | Лист анизотропной электротехнической стали и способ его производства | |
| TWI887859B (zh) | 捲鐵心 | |
| WO2025070790A1 (ja) | 方向性電磁鋼板、及び方向性電磁鋼板の製造方法 | |
| KR20260057218A (ko) | 방향성 전자 강판 및 그 제조 방법 | |
| KR20260057129A (ko) | 방향성 전자 강판 및 그 제조 방법 | |
| KR20260057131A (ko) | 방향성 전자 강판, 및 방향성 전자 강판의 제조 방법 | |
| CN121511319A (zh) | 方向性电磁钢板 | |
| KR20220070293A (ko) | 방향성 전기 강판 및 그 제조 방법 | |
| JP5884168B2 (ja) | 方向性電磁鋼板およびその製造方法 | |
| JP2021169656A (ja) | 方向性電磁鋼板、方向性電磁鋼板の磁区構造の解析方法及び解析システム |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| WWE | Wipo information: entry into national phase |
Ref document number: 2024551524 Country of ref document: JP |
|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 24797198 Country of ref document: EP Kind code of ref document: A1 |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 202517097384 Country of ref document: IN |
|
| ENP | Entry into the national phase |
Ref document number: 1020257034995 Country of ref document: KR Free format text: ST27 STATUS EVENT CODE: A-0-1-A10-A15-NAP-PA0105 (AS PROVIDED BY THE NATIONAL OFFICE) |
|
| WWE | Wipo information: entry into national phase |
Ref document number: KR1020257034995 Country of ref document: KR Ref document number: 1020257034995 Country of ref document: KR |
|
| REG | Reference to national code |
Ref country code: BR Ref legal event code: B01A Ref document number: 112025022970 Country of ref document: BR |
|
| WWP | Wipo information: published in national office |
Ref document number: 202517097384 Country of ref document: IN |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2025128937 Country of ref document: RU Ref document number: 2024797198 Country of ref document: EP |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 2024797198 Country of ref document: EP Effective date: 20251127 |
|
| WWP | Wipo information: published in national office |
Ref document number: 1020257034995 Country of ref document: KR |
|
| ENP | Entry into the national phase |
Ref document number: 2024797198 Country of ref document: EP Effective date: 20251127 |
|
| ENP | Entry into the national phase |
Ref document number: 2024797198 Country of ref document: EP Effective date: 20251127 |
|
| ENP | Entry into the national phase |
Ref document number: 2024797198 Country of ref document: EP Effective date: 20251127 |
|
| WWP | Wipo information: published in national office |
Ref document number: 2025128937 Country of ref document: RU |
|
| ENP | Entry into the national phase |
Ref document number: 2024797198 Country of ref document: EP Effective date: 20251127 |
|
| ENP | Entry into the national phase |
Ref document number: 2024797198 Country of ref document: EP Effective date: 20251127 |
|
| ENP | Entry into the national phase |
Ref document number: 2024797198 Country of ref document: EP Effective date: 20251127 |
|
| ENP | Entry into the national phase |
Ref document number: 2024797198 Country of ref document: EP Effective date: 20251127 |
|
| ENP | Entry into the national phase |
Ref document number: 2024797198 Country of ref document: EP Effective date: 20251127 |
|
| WWP | Wipo information: published in national office |
Ref document number: 2024797198 Country of ref document: EP |