CN111925192A - 一种基于3d打印技术制备钛酸铝-氧化镁复相陶瓷的方法 - Google Patents
一种基于3d打印技术制备钛酸铝-氧化镁复相陶瓷的方法 Download PDFInfo
- Publication number
- CN111925192A CN111925192A CN202010776032.6A CN202010776032A CN111925192A CN 111925192 A CN111925192 A CN 111925192A CN 202010776032 A CN202010776032 A CN 202010776032A CN 111925192 A CN111925192 A CN 111925192A
- Authority
- CN
- China
- Prior art keywords
- magnesium oxide
- aluminum titanate
- printing
- oxide composite
- composite ceramics
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B35/00—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/01—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products based on oxide ceramics
- C04B35/03—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products based on oxide ceramics based on magnesium oxide, calcium oxide or oxide mixtures derived from dolomite
- C04B35/04—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products based on oxide ceramics based on magnesium oxide, calcium oxide or oxide mixtures derived from dolomite based on magnesium oxide
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B1/00—Producing shaped prefabricated articles from the material
- B28B1/001—Rapid manufacturing of 3D objects by additive depositing, agglomerating or laminating of material
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B35/00—Shaped ceramic products characterised by their composition; Ceramics compositions; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/622—Forming processes; Processing powders of inorganic compounds preparatory to the manufacturing of ceramic products
- C04B35/626—Preparing or treating the powders individually or as batches ; preparing or treating macroscopic reinforcing agents for ceramic products, e.g. fibres; mechanical aspects section B
- C04B35/62605—Treating the starting powders individually or as mixtures
- C04B35/6261—Milling
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/30—Constituents and secondary phases not being of a fibrous nature
- C04B2235/32—Metal oxides, mixed metal oxides, or oxide-forming salts thereof, e.g. carbonates, nitrates, (oxy)hydroxides, chlorides
- C04B2235/3201—Alkali metal oxides or oxide-forming salts thereof
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/30—Constituents and secondary phases not being of a fibrous nature
- C04B2235/32—Metal oxides, mixed metal oxides, or oxide-forming salts thereof, e.g. carbonates, nitrates, (oxy)hydroxides, chlorides
- C04B2235/3224—Rare earth oxide or oxide forming salts thereof, e.g. scandium oxide
- C04B2235/3225—Yttrium oxide or oxide-forming salts thereof
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/30—Constituents and secondary phases not being of a fibrous nature
- C04B2235/32—Metal oxides, mixed metal oxides, or oxide-forming salts thereof, e.g. carbonates, nitrates, (oxy)hydroxides, chlorides
- C04B2235/3231—Refractory metal oxides, their mixed metal oxides, or oxide-forming salts thereof
- C04B2235/3232—Titanium oxides or titanates, e.g. rutile or anatase
- C04B2235/3234—Titanates, not containing zirconia
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/30—Constituents and secondary phases not being of a fibrous nature
- C04B2235/34—Non-metal oxides, non-metal mixed oxides, or salts thereof that form the non-metal oxides upon heating, e.g. carbonates, nitrates, (oxy)hydroxides, chlorides
- C04B2235/3418—Silicon oxide, silicic acids or oxide forming salts thereof, e.g. silica sol, fused silica, silica fume, cristobalite, quartz or flint
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/50—Constituents or additives of the starting mixture chosen for their shape or used because of their shape or their physical appearance
- C04B2235/54—Particle size related information
- C04B2235/5418—Particle size related information expressed by the size of the particles or aggregates thereof
- C04B2235/5445—Particle size related information expressed by the size of the particles or aggregates thereof submicron sized, i.e. from 0,1 to 1 micron
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/02—Composition of constituents of the starting material or of secondary phases of the final product
- C04B2235/50—Constituents or additives of the starting mixture chosen for their shape or used because of their shape or their physical appearance
- C04B2235/54—Particle size related information
- C04B2235/5418—Particle size related information expressed by the size of the particles or aggregates thereof
- C04B2235/5454—Particle size related information expressed by the size of the particles or aggregates thereof nanometer sized, i.e. below 100 nm
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/60—Aspects relating to the preparation, properties or mechanical treatment of green bodies or pre-forms
- C04B2235/602—Making the green bodies or pre-forms by moulding
- C04B2235/6026—Computer aided shaping, e.g. rapid prototyping
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/70—Aspects relating to sintered or melt-casted ceramic products
- C04B2235/74—Physical characteristics
- C04B2235/77—Density
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2235/00—Aspects relating to ceramic starting mixtures or sintered ceramic products
- C04B2235/70—Aspects relating to sintered or melt-casted ceramic products
- C04B2235/96—Properties of ceramic products, e.g. mechanical properties such as strength, toughness, wear resistance
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Ceramic Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Materials Engineering (AREA)
- Structural Engineering (AREA)
- Organic Chemistry (AREA)
- Inorganic Chemistry (AREA)
- Mechanical Engineering (AREA)
- Compositions Of Oxide Ceramics (AREA)
Abstract
本发明方法将复相陶瓷材料制备方法与3D成型打印技术相结合,并选择合理的氧化镁颗粒和钛酸铝颗粒级配方式,经陶瓷浆料制备、模型设计与切片软件处理、3D打印成型、烧结的工序,制备高性能的钛酸铝‑氧化镁复相陶瓷。本发明合理级配,增加空间利用率,提高其致密度和力学性能。向氧化镁陶瓷中引入钛酸铝粉体,起到钉扎和裂纹偏转的增韧作用,并细化晶粒,抑制异常晶粒的长大,改善氧化镁陶瓷的抗热震性能。同时,在利用3D打印技术成型过程中,不需要金属模具而降低成本,简化制备工艺,成型尺寸精度高,提高生产效率。
Description
技术领域
本发明属于高温结构复相陶瓷领域,具体涉及一种基于3D打印技术制备钛酸铝-氧化镁复相陶瓷的方法。
背景技术
氧化镁陶瓷作为一种高温结构陶瓷,具有高熔点、良好的体积稳定性、优良的抗高温蠕变性、对碱性金属熔渣有较强的抗侵蚀等诸多的特性,广泛作为冶炼金属的坩埚材料、高温热电偶的保护管材料、高温炉的炉衬材料等。但是,在氧化镁坯体烧结过程中,由于其热膨胀系数大、弹性模量大,氧化镁陶瓷表现出烧结性能欠佳,抗热震性能差的缺陷,难以满足现代高温工业发展的要求,制约其进一步推广使用。
在传统的氧化镁陶瓷制备过程中,往往引入烧结助剂能够有效地促进氧化镁陶瓷致密化,降低烧结温度,以及改善抗热震性能。如专利上公开申请号“CN201811629363.6”的名称为“一种氧化镁陶瓷粉体及其制备方法”,其在氧化镁陶瓷制备过程中,使用稀土氧化物和五氧化二钒等烧结助剂,制备高性能的氧化镁陶瓷,其断裂模数达到65-74MPa。但是,烧结助剂的使用也存在两方面不足:一方面,在烧结过程时,不易多加烧结助剂,否则,烧结助剂在高温下熔化形成大量玻璃态的液相,降低氧化镁陶瓷的高温使用性能,影响氧化镁陶瓷的使用强度。另一方面,烧结助剂能与氧化镁形成第二相或固溶体,形成的第二相或固溶体与方镁石相之间的热膨胀系数有差异较大,在冷热交替环境中易形成热应力,从而造成氧化镁陶瓷表面出现开裂、剥落,并不断发展,最终使材料失效,影响氧化镁陶瓷的使用寿命。目前,钛酸铝作为一种富有潜力的高温低膨胀添加剂,这是由于其具有高熔点、优良的抗热震性能、低的导热系数等性能,并可充当第二相质点而细化晶粒,进一步提高材料的力学性能。
传统的氧化镁成型方法有注浆成型、流延成型、挤压成型、冷等静压成型、热等静压成型等,如专利上公开申请号“CN201910342863.X”的名称为“一种氧化镁陶瓷型芯及其制备方法”,其以氧化镁和二氧化钛为原料,经模具受压成型制备复相材料的坯体,暴露其制备温度高、成型困难、加工性差等局限性。然而,3D打印成型技术作为今年来快速兴起的成型技术,其融合了计算机辅助设计、材料加工与成型技术,通过软件与数控系统将陶瓷浆料按照逐层堆积方式,制造出所需要大小和形状的陶瓷。该技术优势在于,生产效率高,材料利用率高,生产周期短,成型精度高,尤其是解决了其不受零件形状复杂程度限制无需成型模具和复杂的处理过程。
发明内容
本发明针对现有技术制备氧化镁陶瓷的烧结性能欠佳、抗热震性能差、力学强度较差以及成型率低的缺点及不足,提供一种基于3D打印技术制备钛酸铝-氧化镁复相陶瓷的方法,该方法提高钛酸铝-氧化镁复相陶瓷的致密度,改善烧结性能和抗热震性能,进而增强其力学强度,其利用3D打印成型技术,工艺步骤简单,生产成本降低,具有较高的设计价值。
一种基于3D打印技术制备钛酸铝-氧化镁复相陶瓷的方法,其特征在于,具体操作步骤如下:
(1)以质量百分比计,将70-90%的氧化镁粉体,5-25%的钛酸铝粉体,5-10%的烧结助剂,放入球磨机中湿磨5-15h,得陶瓷浆料;
(2)利用建模软件建立打印试样的模型,再利用陶瓷3D打印切片软件将stl格式转化为gcode格式,并将文件存入到3D打印机中,进行切片打印;
(3)将陶瓷浆料注入3D打印设备的料管中,打开气泵,陶瓷浆料将从打印喷嘴中挤出并沉积在工作台,进行逐层打印,获得打印坯体;
(4)将打印坯体置于1300-1500℃高温炉中烧结并保温2-8h,即得钛酸铝-氧化镁复相陶瓷。
所述步骤(1)中,氧化镁粉体的粒度为180-250nm,其中MgO含量≥80%,钛酸铝粉体的粒度为50-80nm,Al2TiO5含量≥80%,烧结助剂的粒度为50-80nm。
所述步骤(1)中,烧结助剂为氧化钇、二氧化硅或碱性金属氧化物中的任一种。
与现有技术相比,本发明的有益效果是:1)本发明对原料的粒度进行了合理选择,在球磨过程中,氧化镁粉体颗粒与钛酸铝粉体颗粒间形成良好的粒度级配,具有相对较窄的粒度分布和更好的流动性,增加空间利用率,提高其致密度和力学性能,并使在3D打印成型过程中两种不同的陶瓷基体间具有更好的结合性和相容性;2)采用钛酸铝粉体作为添加剂,均匀分布于氧化镁颗粒三相交界处,起到钉扎和裂纹偏转的增韧作用,并细化晶粒,抑制异常晶粒的长大,改善氧化镁陶瓷的抗热震性能;3)在利用3D打印技术成型过程中,不需要金属模具而降低成本,简化制备工艺,成型尺寸精度高,提高生产效率,制备高性能的钛酸铝-氧化镁复相陶瓷。
附图说明
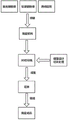
图1所示为本发明实施例制备钛酸铝-氧化镁复相陶瓷的工艺流程图。
具体实施方式
下面将结合本发明实施例中的附图,对本发明实施例中的技术方案进行清楚、完整地描述,显然,所描述的实施例仅仅是本发明一部分实施例,而不是全部的实施例。基于本发明中的实施例,本领域普通技术人员在没有做出创造性劳动前提下所获得的所有其他实施例,都属于本发明保护的范围。
实施例1
将750g粒度200nm氧化镁粉,200g粒度50nm钛酸铝粉,50g粒度50nm的氧化钇,放入球磨机中湿磨6h,得陶瓷浆料;利用建模软件建立打印试样的模型,再利用陶瓷3D打印切片软件将stl格式转化为gcode格式,并将文件存入到3D打印机中,进行切片打印;将陶瓷浆料注入3D打印设备的料管中,打开气泵,陶瓷浆料将从打印喷嘴中挤出并沉积在工作台,进行逐层打印,获得打印坯体;将打印坯体置于1350℃高温炉中烧结并保温4h,即得钛酸铝-氧化镁复相陶瓷。
本实施例制备的钛酸铝-氧化镁复相陶瓷的体积密度3.36g/cm3,气孔率4.2%,常温抗折强度145MPa,热震次数8次
实施例2
将850g粒度185nm氧化镁粉,100g粒度60nm钛酸铝粉,50g粒度60nm的二氧化硅,放入球磨机中湿磨5h,得陶瓷浆料;利用建模软件建立打印试样的模型,再利用陶瓷3D打印切片软件将stl格式转化为gcode格式,并将文件存入到3D打印机中,进行切片打印;将陶瓷浆料注入3D打印设备的料管中,打开气泵,陶瓷浆料将从打印喷嘴中挤出并沉积在工作台,进行逐层打印,获得打印坯体;将打印坯体置于1400℃高温炉中烧结并保温2h,即得钛酸铝-氧化镁复相陶瓷。
本实施例制备的钛酸铝-氧化镁复相陶瓷的体积密度3.45g/cm3,气孔率2.6%,常温抗折强度168MPa,热震次数6次
实施例3
将900g粒度240nm氧化镁粉,50g粒度55nm钛酸铝粉,50g粒度55nm的二氧化硅,放入球磨机中湿磨10h,得陶瓷浆料;利用建模软件建立打印试样的模型,再利用陶瓷3D打印切片软件将stl格式转化为gcode格式,并将文件存入到3D打印机中,进行切片打印;将陶瓷浆料注入3D打印设备的料管中,打开气泵,陶瓷浆料将从打印喷嘴中挤出并沉积在工作台,进行逐层打印,获得打印坯体;将打印坯体置于1450℃高温炉中烧结并保温5h,即得钛酸铝-氧化镁复相陶瓷。
本实施例制备的钛酸铝-氧化镁复相陶瓷的体积密度3.5g/cm3,气孔率1.8%,常温抗折强度176MPa,热震次数5次
尽管已经示出和描述了本发明的实施例,对于本领域的普通技术人员而言,可以理解在不脱离本发明的原理和精神的情况下可以对这些实施例进行多种变化、修改、替换和变型,本发明的范围由所附权利要求及其等同物限定。
Claims (3)
1.一种基于3D打印技术制备钛酸铝-氧化镁复相陶瓷的方法,其特征在于,具体操作步骤如下:
(1)以质量百分比计,将70-90%的氧化镁粉体,5-25%的钛酸铝粉体,5-10%的烧结助剂,放入球磨机中湿磨5-15h,得陶瓷浆料;
(2)利用建模软件建立打印试样的模型,再利用陶瓷3D打印切片软件将stl格式转化为gcode格式,并将文件存入到3D打印机中,进行切片打印;
(3)将陶瓷浆料注入3D打印设备的料管中,打开气泵,陶瓷浆料将从打印喷嘴中挤出并沉积在工作台,进行逐层打印,获得打印坯体;
(4)将打印坯体置于1300-1500℃高温炉中烧结并保温2-8h,即得钛酸铝-氧化镁复相陶瓷。
2.根据权利要求1所述一种基于3D打印技术制备钛酸铝-氧化镁复相陶瓷的方法,其特征在于,所述步骤(1)中,氧化镁粉体的粒度为180-250nm,其中MgO含量≥80%,钛酸铝粉体的粒度为50-80nm,Al2TiO5含量≥80%,烧结助剂的粒度为50-80nm。
3.根据权利要求1所述一种基于3D打印技术制备钛酸铝-氧化镁复相陶瓷的方法,其特征在于,所述步骤(1)中,烧结助剂为氧化钇、二氧化硅或碱性金属氧化物中的任一种。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010776032.6A CN111925192A (zh) | 2020-08-05 | 2020-08-05 | 一种基于3d打印技术制备钛酸铝-氧化镁复相陶瓷的方法 |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010776032.6A CN111925192A (zh) | 2020-08-05 | 2020-08-05 | 一种基于3d打印技术制备钛酸铝-氧化镁复相陶瓷的方法 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN111925192A true CN111925192A (zh) | 2020-11-13 |
Family
ID=73306488
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010776032.6A Pending CN111925192A (zh) | 2020-08-05 | 2020-08-05 | 一种基于3d打印技术制备钛酸铝-氧化镁复相陶瓷的方法 |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN111925192A (zh) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112759415A (zh) * | 2020-12-31 | 2021-05-07 | 松山湖材料实验室 | 多孔陶瓷的制备工艺 |
| CN117776676A (zh) * | 2024-02-26 | 2024-03-29 | 上海南极星高科技股份有限公司 | 光固化3d打印工艺制备氧化镁多孔陶瓷的方法 |
| CN118637892A (zh) * | 2024-07-02 | 2024-09-13 | 辽宁玻陶科技有限公司 | 一种氧化镁陶瓷的制造方法 |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01249657A (ja) * | 1988-03-31 | 1989-10-04 | Toshiba Corp | セラミックス焼結体 |
| CN104526838A (zh) * | 2014-12-30 | 2015-04-22 | 宁波伏尔肯机械密封件制造有限公司 | 陶瓷3d打印成型的方法 |
| CN107098717A (zh) * | 2017-04-07 | 2017-08-29 | 武汉理工大学 | 一种过滤用多孔陶瓷的三维打印成型制备方法 |
| CN107500781A (zh) * | 2017-09-28 | 2017-12-22 | 上海应用技术大学 | 一种多孔陶瓷的制备方法 |
| CN111018495A (zh) * | 2019-12-24 | 2020-04-17 | 辽宁科技大学 | 一种钛酸铝增强方镁石复相陶瓷材料 |
| CN111205072A (zh) * | 2020-02-27 | 2020-05-29 | 辽宁科技大学 | 一种3d打印镁铝质熔融金属过滤装置的制备方法 |
-
2020
- 2020-08-05 CN CN202010776032.6A patent/CN111925192A/zh active Pending
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH01249657A (ja) * | 1988-03-31 | 1989-10-04 | Toshiba Corp | セラミックス焼結体 |
| CN104526838A (zh) * | 2014-12-30 | 2015-04-22 | 宁波伏尔肯机械密封件制造有限公司 | 陶瓷3d打印成型的方法 |
| CN107098717A (zh) * | 2017-04-07 | 2017-08-29 | 武汉理工大学 | 一种过滤用多孔陶瓷的三维打印成型制备方法 |
| CN107500781A (zh) * | 2017-09-28 | 2017-12-22 | 上海应用技术大学 | 一种多孔陶瓷的制备方法 |
| CN111018495A (zh) * | 2019-12-24 | 2020-04-17 | 辽宁科技大学 | 一种钛酸铝增强方镁石复相陶瓷材料 |
| CN111205072A (zh) * | 2020-02-27 | 2020-05-29 | 辽宁科技大学 | 一种3d打印镁铝质熔融金属过滤装置的制备方法 |
Non-Patent Citations (2)
| Title |
|---|
| 刘维良: "《先进陶瓷工艺学》", 31 August 2004, 武汉理工大学出版社 * |
| 宋晓岚等: "《无机材料工艺学》", 30 September 2007, 冶金工业出版社 * |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112759415A (zh) * | 2020-12-31 | 2021-05-07 | 松山湖材料实验室 | 多孔陶瓷的制备工艺 |
| CN117776676A (zh) * | 2024-02-26 | 2024-03-29 | 上海南极星高科技股份有限公司 | 光固化3d打印工艺制备氧化镁多孔陶瓷的方法 |
| CN117776676B (zh) * | 2024-02-26 | 2024-06-04 | 上海南极星高科技股份有限公司 | 光固化3d打印工艺制备氧化镁多孔陶瓷的方法 |
| CN118637892A (zh) * | 2024-07-02 | 2024-09-13 | 辽宁玻陶科技有限公司 | 一种氧化镁陶瓷的制造方法 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN104874768B (zh) | 一种利用3d打印空间结构制备金属基复合材料的方法 | |
| CN102531648B (zh) | 一种钛合金铸造用氧化钙基陶瓷型芯及其制备方法 | |
| JP2022532847A (ja) | 低融点酸化物による腐食を防止する希土類タンタル酸塩セラミックス及びその製造方法 | |
| CN103951394B (zh) | 一种高温抗热震氧化铝陶瓷承烧板及其制备工艺 | |
| CN103833403B (zh) | 一种碳化硅晶须增韧碳化硼陶瓷复合材料的制备方法及产品 | |
| CN103586296B (zh) | 一种镶拼式陶瓷拉丝模及其制备方法 | |
| CN103833383B (zh) | 一种闭孔结构的刚玉-镁铝尖晶石质耐火骨料的制备方法 | |
| CN106316369A (zh) | 一种3d打印陶瓷坯体的排胶和烧结工艺 | |
| CN114716260B (zh) | 一种陶瓷-金属复合材料与金属材料的连接件及其制备方法 | |
| CN103030413B (zh) | 一种刚玉莫来石坩埚的制备方法 | |
| CN103232245A (zh) | 晶硅切割废弃料制备氮化硅复合碳化硅陶瓷的方法 | |
| CN105272181A (zh) | 复合陶瓷型芯的制备工艺 | |
| CN107640963A (zh) | 一种梯度陶瓷型芯材料的制备方法 | |
| CN103739289A (zh) | 碳化硅陶瓷热电偶保护管及其制备方法 | |
| CN104310976A (zh) | 一种高耐磨耐高温陶瓷 | |
| CN115925417A (zh) | 一种低热导抗cmas腐蚀高熵锆酸盐陶瓷材料及其制备方法与应用 | |
| CN104844199B (zh) | 注浆法制备氧化锆-硼化锆双层复合陶瓷发热体的工艺 | |
| CN113443919A (zh) | 一种非晶态合金喷嘴材料及其制备方法 | |
| CN106478081A (zh) | 真空碳热还原强化熔融石英高温性能的方法 | |
| CN102173831B (zh) | 流延法制备层状硼化锆超高温陶瓷的方法 | |
| CN101423383A (zh) | 一种低温烧成陶瓷辊棒及其制备方法 | |
| CN102173827B (zh) | 硼化锆-碳化硅/氮化硼层状超高温陶瓷的制备方法 | |
| CN102419094A (zh) | 立式中频炉整体浇铸复合炉胆和保温层的制备方法 | |
| CN101182212A (zh) | YAG/ZrB2系复相陶瓷及其制备方法 | |
| CN100450971C (zh) | 一种Al-AlN-ZrO2陶瓷材料的制备方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| RJ01 | Rejection of invention patent application after publication |
Application publication date: 20201113 |
|
| RJ01 | Rejection of invention patent application after publication |