CN114277452B - Dry-jet wet spinning spinning equipment - Google Patents
Dry-jet wet spinning spinning equipment Download PDFInfo
- Publication number
- CN114277452B CN114277452B CN202210092875.3A CN202210092875A CN114277452B CN 114277452 B CN114277452 B CN 114277452B CN 202210092875 A CN202210092875 A CN 202210092875A CN 114277452 B CN114277452 B CN 114277452B
- Authority
- CN
- China
- Prior art keywords
- spinning
- pipeline
- dry
- jet wet
- fine
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000009987 spinning Methods 0.000 title claims abstract description 127
- 238000002166 wet spinning Methods 0.000 title claims abstract description 40
- 238000001816 cooling Methods 0.000 claims abstract description 22
- 238000005345 coagulation Methods 0.000 claims abstract description 18
- 230000015271 coagulation Effects 0.000 claims abstract description 16
- 230000000712 assembly Effects 0.000 claims abstract description 13
- 238000000429 assembly Methods 0.000 claims abstract description 13
- 239000000155 melt Substances 0.000 claims abstract description 13
- 238000000034 method Methods 0.000 claims description 34
- 238000007664 blowing Methods 0.000 claims description 14
- 238000009413 insulation Methods 0.000 claims description 12
- 238000004321 preservation Methods 0.000 claims description 10
- 238000009826 distribution Methods 0.000 claims description 8
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 7
- 239000007788 liquid Substances 0.000 claims 1
- 238000004519 manufacturing process Methods 0.000 abstract description 21
- 239000000835 fiber Substances 0.000 abstract description 3
- 239000000126 substance Substances 0.000 abstract description 3
- 238000007711 solidification Methods 0.000 abstract 1
- 230000008023 solidification Effects 0.000 abstract 1
- 238000007378 ring spinning Methods 0.000 description 6
- 238000012986 modification Methods 0.000 description 5
- 230000004048 modification Effects 0.000 description 5
- 238000010276 construction Methods 0.000 description 2
- 238000010586 diagram Methods 0.000 description 2
- 230000000694 effects Effects 0.000 description 2
- 239000012530 fluid Substances 0.000 description 2
- 239000007921 spray Substances 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 230000002349 favourable effect Effects 0.000 description 1
Images


Landscapes
- Spinning Methods And Devices For Manufacturing Artificial Fibers (AREA)
Abstract
本发明提供一种干喷湿纺法纺丝设备,属于化学纤维制造工程技术领域。其包括熔体管路、多个喷丝组件、冷却风管路、凝固浴槽、和集束导丝棒,熔体管路包括第一种主管路和多个第一种支管路,第一种主管路与第一种支管路分别连通;第一种支管路与喷丝组件一一对应,并且,第一种支管路与对应的喷丝组件连通,使得经过多个喷丝组件之后,纺丝熔体形成多组纺丝细流;冷却风管路用于通过多向出风口向多组纺丝细流吹风;集束导丝棒设置于凝固浴槽内,使得多组纺丝细流经过集束导丝棒后完成集束导丝。应用其进行纺丝,产能为原纺丝设备纺丝产能的两倍,并且,在相同产能的生产线条件下,投资成本和占地面积均有所降低。
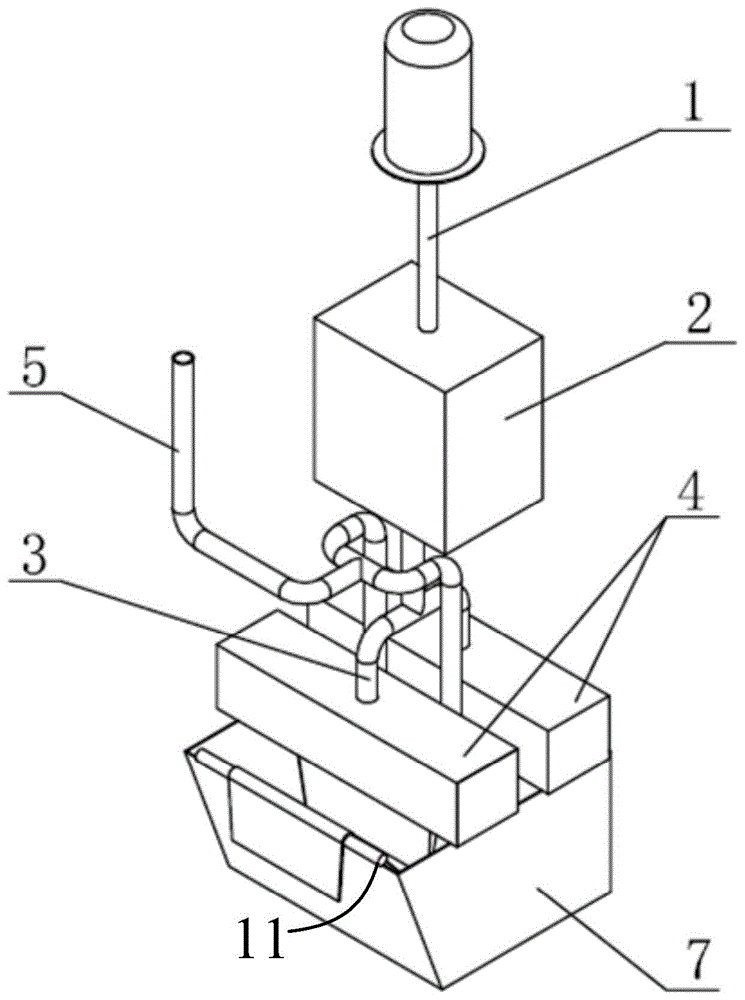
The invention provides a dry-jet wet-spinning spinning device, which belongs to the technical field of chemical fiber manufacturing engineering. It includes a melt pipeline, a plurality of spinneret assemblies, a cooling air pipeline, a solidification bath, and a cluster guide wire rod. The melt pipeline includes a first-type main pipeline and a plurality of first-type branch pipelines. The first-type main pipe The first branch pipeline is connected with the first kind of branch pipeline respectively; the first kind of branch pipeline is in one-to-one correspondence with the spinneret assembly, and the first kind of branch pipeline is connected with the corresponding spinneret assembly, so that after passing through a plurality of spinneret assemblies, the spinning melt multiple groups of spinning fine streams; the cooling air pipeline is used to blow air to multiple groups of spinning fine streams through multi-directional air outlets; the cluster guide rod is set in the coagulation bath so that multiple groups of spinning streams pass through the cluster guide wires After the rod completes the bundled guidewire. When it is used for spinning, the production capacity is twice that of the original spinning equipment, and, under the conditions of the production line with the same production capacity, the investment cost and floor area are both reduced.
Description
技术领域technical field
本发明涉及化学纤维制造工程技术领域,特别是涉及一种干喷湿纺法纺丝设备。The invention relates to the technical field of chemical fiber manufacturing engineering, in particular to a dry-jet wet spinning spinning equipment.
背景技术Background technique
干喷湿纺法纺丝是20世纪60年代逐渐发展起来的一种纺丝方法,在化纤工业中有广泛的应用。现有技术中工业化的干喷湿纺法纺丝设备主要有两种形式,一种为长条形喷丝板配合侧吹风,一种是环形喷丝板配合环形吹风两种形式,各有优缺点。然而,现有技术中的干喷湿纺法纺丝设备难以兼顾上述两种形式的优点。Dry-jet wet spinning is a spinning method gradually developed in the 1960s, and it is widely used in the chemical fiber industry. In the prior art, there are mainly two forms of industrialized dry-jet wet spinning spinning equipment, one is a strip-shaped spinneret with side blowing, and the other is an annular spinneret with annular blowing. Each has its own advantages and disadvantages. shortcoming. However, it is difficult for the dry-jet wet spinning method spinning equipment in the prior art to take into account the advantages of the above two forms.
发明内容Contents of the invention
有鉴于此,本发明提供了一种干喷湿纺法纺丝设备,应用其进行纺丝,产能为原纺丝设备纺丝产能的两倍,并且,在相同产能的生产线条件下,投资成本和占地面积均有所降低,从而更加适于实用。In view of this, the present invention provides a kind of dry-jet wet-spinning method spinning equipment, uses it to spin, and the production capacity is twice of the spinning production capacity of the original spinning equipment, and, under the production line condition of the same production capacity, the investment cost The size and footprint are reduced, making it more suitable for practical use.
为了达到上述目的,本发明提供的干喷湿纺法纺丝设备的技术方案如下:In order to achieve the above object, the technical scheme of the dry jet wet spinning method spinning equipment provided by the invention is as follows:
本发明提供的干喷湿纺法纺丝设备包括熔体管路(3)、多个喷丝组件(4)、冷却风管路(5)、凝固浴槽(7)、和集束导丝棒,The dry-jet wet spinning spinning equipment provided by the present invention comprises a melt pipeline (3), a plurality of spinneret assemblies (4), a cooling air pipeline (5), a coagulation bath (7), and a cluster guide wire rod,
所述熔体管路(3)包括第一种主管路和多个第一种支管路,所述第一种主管路与所述第一种支管路分别连通;The melt pipeline (3) includes a first-type main pipeline and a plurality of first-type branch pipelines, and the first-type main pipeline communicates with the first-type branch pipelines respectively;
所述第一种支管路与所述喷丝组件(4)一一对应,并且,所述第一种支管路与对应的喷丝组件(4)连通,使得经过所述多个喷丝组件(4)之后,纺丝熔体形成多组纺丝细流;The first branch pipeline corresponds to the spinner assembly (4) one by one, and the first branch pipeline communicates with the corresponding spinneret assembly (4), so that passing through the multiple spinneret assemblies ( 4) Afterwards, the spinning melt forms multiple groups of fine spinning streams;
所述冷却风管路(5)用于通过出风口向所述多组纺丝细流吹风;The cooling air pipeline (5) is used to blow air to the multiple groups of fine spinning streams through the air outlet;
所述集束导丝棒设置于所述凝固浴槽(7)内,使得所述多组纺丝细流经过所述集束导丝棒后完成集束导丝。The clustering guide rods are arranged in the coagulation bath (7), so that the multiple groups of fine spinning streams pass through the clustering guide rods to complete the clustering guide rods.
本发明提供的干喷湿纺法纺丝设备还可采用以下技术措施进一步实现。The dry-jet wet spinning method spinning equipment provided by the present invention can also be further realized by adopting the following technical measures.
作为优选,所述多个喷丝组件(4)的规格相同;所述多个第一种支管路规格相同。Preferably, the specifications of the multiple spinner assemblies (4) are the same; the specifications of the multiple first branch pipelines are the same.
作为优选,所述干喷湿纺法纺丝设备还包括计量泵(1)和计量泵箱体(2),As preferably, the dry-jet wet spinning method spinning equipment also includes a metering pump (1) and a metering pump casing (2),
纺丝熔体经过所述计量泵(1)和所述计量泵箱体(2)之后进入所述熔体管路(3)。The spinning melt enters the melt pipeline (3) after passing through the metering pump (1) and the metering pump casing (2).
作为优选,所述冷却风管路(5)包括第二种主管路和多个第二种支管路,所述第二种主管路与所述多个第二种支管路分别连通。Preferably, the cooling air pipeline (5) includes a second-type main pipeline and multiple second-type branch pipelines, and the second-type main pipeline communicates with the multiple second-type branch pipelines respectively.
作为优选,所述干喷湿纺法纺丝设备还包括冷却风分配吹风装置(6),As preferably, the dry-jet wet spinning method spinning equipment also includes a cooling air distribution blowing device (6),
所述冷却风分配吹风装置(6)包括腔体,所述腔体上设置有所述出风口;The cooling air distribution and blowing device (6) includes a cavity, and the cavity is provided with the air outlet;
所述多个第二种支管路分别与所述腔体连通。The multiple second-type branch pipelines are respectively communicated with the cavity.
作为优选,所述多个第二种支管路在所述腔体上均匀布置。Preferably, the plurality of branch pipelines of the second type are evenly arranged on the cavity.
作为优选,所述干喷湿纺法纺丝设备还包括两个挡风板(9),As preferably, the dry-jet wet spinning method spinning equipment also includes two windshields (9),
所述两个挡风板(9)分别设置于所述腔体的轴向两端下方,The two windshields (9) are respectively arranged below the two axial ends of the cavity,
所述挡风板(9)在水平方向的伸出长度超过所述纺丝流体的最远端,所述挡风板(9)的最底端处于所述凝固浴槽(7)的凝固浴液面以下。The protruding length of the windshield (9) in the horizontal direction exceeds the farthest end of the spinning fluid, and the bottommost end of the windshield (9) is in the coagulation bath of the coagulation bath (7). below the face.
作为优选,所述干喷湿纺法纺丝设备还包括保温夹套,所述保温夹套设置于所述熔体管路(3)和/或多个喷丝组件(4)的外围。Preferably, the dry-jet wet-spinning spinning equipment further includes a thermal insulation jacket, and the thermal insulation jacket is arranged on the periphery of the melt pipeline (3) and/or the plurality of spinning assemblies (4).
作为优选,所述干喷湿纺法纺丝设备还包括保温夹套,所述保温夹套设置于所述计量泵箱体(2)的外围。Preferably, the dry-jet wet-spinning spinning equipment further includes a thermal insulation jacket, and the thermal insulation jacket is arranged on the periphery of the metering pump box (2).
作为优选,所述保温夹套内设置有介质腔,所述介质腔内充有保温介质。As a preference, a medium cavity is provided inside the heat preservation jacket, and the medium cavity is filled with heat preservation medium.
作为优选,所述保温介质为水,通过控制水温实现温度控制。Preferably, the heat preservation medium is water, and the temperature control is realized by controlling the temperature of the water.
作为优选,所述干喷湿纺法纺丝设备还包括转向棒(11),所述转向棒(11)设置于所述凝固浴槽(7)的出口边缘,As preferably, the spinning equipment of the dry-jet wet spinning method also includes a turning rod (11), and the turning rod (11) is arranged on the outlet edge of the coagulation bath (7),
完成集束导丝的纺丝细流经过所述转向棒(11)后完成纺丝过程。The fine spinning stream of the bundled guide yarn passes through the turning rod (11) to complete the spinning process.
作为优选,As a preference,
所述集束导丝棒包括第一集束导丝棒(10),所述多组纺丝细流均通过所述第一集束导丝棒(10)完成集束导丝。The clustering guide rods include a first clustering guide rod (10), and the plurality of groups of fine spinning streams all pass through the first clustering guide rods (10) to complete the clustering guide rods.
作为优选,As a preference,
所述集束导丝棒包括第多根集束导丝棒,The clustering guide wire rods include a first clustering guide wire rods,
所述多组纺丝细流中每组纺丝细流均至少经过一根集束导丝棒后完成集束导丝。Each group of spinning fine streams in the plurality of groups of spinning fine streams passes through at least one clustering guide rod to complete clustering guide wires.
本发明提供的干喷湿法纺丝设备采用了多套长条形喷丝板组件,所以与普通长条板纺丝设备相比,喷丝孔的数量为原来的多倍。在相同的纺速下,纺丝机产能为原纺丝机的多倍。在相同产能的生产线上采用本设备能够减少设备投资成本,同时减少土建投资成本。The dry-jet wet spinning equipment provided by the present invention adopts multiple sets of elongated spinneret assemblies, so compared with common elongated spinneret equipment, the number of spinneret holes is many times that of the original. At the same spinning speed, the production capacity of the spinning machine is many times that of the original spinning machine. Using this equipment on a production line with the same production capacity can reduce equipment investment costs and reduce civil construction investment costs.
附图说明Description of drawings
通过阅读下文优选实施方式的详细描述,各种其他的优点和益处对于本领域普通技术人员将变得清楚明了。附图仅用于示出优选实施方式的目的,而并不认为是对本发明的限制。而且在整个附图中,用相同的参考符号表示相同的部件。在附图中:Various other advantages and benefits will become apparent to those of ordinary skill in the art upon reading the following detailed description of the preferred embodiment. The drawings are only for the purpose of illustrating a preferred embodiment and are not to be considered as limiting the invention. Also throughout the drawings, the same reference numerals are used to designate the same parts. In the attached picture:
附图1为本发明实施例提供的干喷湿纺法纺丝设备的立体结构示意图;Accompanying
附图2为本发明实施例提供的干喷湿纺法纺丝设备的纵向剖视图,其中,集束导丝棒为一根;Accompanying
附图3为附图2中A部分的局部放大图;Accompanying
附图4为本发明实施例提供的干喷湿纺法纺丝设备中应用的冷却风管路的立体结构示意图;Accompanying
附图5为本发明实施例提供的干喷湿纺法纺丝设备的纵向剖视图,其中,集束导丝棒为两根;Accompanying
附图6为本发明实施例提供的干喷湿纺法纺丝设备的纵向剖视图,其中,集束导丝棒为三根;Accompanying
附图标记说明:Explanation of reference signs:
1-计量泵,2-计量泵箱体,3-熔体管路,4-喷丝组件,5-冷却风管路,6-冷却风分配吹风装置,7-凝固浴槽,8-凝固浴液面,9-挡风板,10-第一集束导丝棒,11-转向棒,12-第二集束导丝棒,13-第三集束导丝棒,14-第四集束导丝棒。1-Metering pump, 2-Metering pump box, 3-Melt pipeline, 4-Spinner assembly, 5-Cooling air pipeline, 6-Cooling air distribution blowing device, 7-Coagulation bath, 8-Coagulation bath Surface, 9-windshield, 10-the first clustering guide wire rod, 11-steering rod, 12-the second clustering guide wire rod, 13-the third clustering guide wire rod, 14-the fourth clustering guide wire rod.
具体实施方式detailed description
有鉴于此,本发明提供了一种干喷湿纺法纺丝设备,应用其进行纺丝,产能为原纺丝设备纺丝产能的两倍,并且,在相同产能的生产线条件下,投资成本和占地面积均有所降低,从而更加适于实用。In view of this, the present invention provides a kind of dry-jet wet-spinning method spinning equipment, uses it to spin, and the production capacity is twice of the spinning production capacity of the original spinning equipment, and, under the production line condition of the same production capacity, the investment cost The size and footprint are reduced, making it more suitable for practical use.
发明人经过艰苦卓绝的努力,发现长条板纺丝设备相对于环形板纺丝设备的劣势和优势主要包括:After arduous efforts, the inventor found that the disadvantages and advantages of the long strip spinning equipment compared with the ring spinning equipment mainly include:
首先,长条板纺丝设备相对于环形板纺丝设备的劣势主要包括,First of all, the disadvantages of strip spinning equipment compared to ring spinning equipment mainly include:
第一,长条板纺丝设备与环形板纺丝设备相比,设备单位占地面积上的喷丝孔数量约为后者的一半。相同纺速下,孔数决定了产能。所以长条板纺丝设备单位产能的占地面积较环形板纺丝设备大。这就造成其在设备数量上和土建投资上的成本劣势。First, compared with the annular plate spinning equipment, the number of spinneret holes in the equipment unit area is about half of the latter. At the same spinning speed, the number of holes determines the production capacity. Therefore, the unit production area of the strip spinning equipment is larger than that of the ring spinning equipment. This causes its cost disadvantage in terms of equipment quantity and civil construction investment.
第二,长条板纺丝设备的侧吹风方式造成纺丝细流在丝束带的端部和中间部分所接触到的风场不均匀。而环形纺丝设备采用环形吹风,由内而外四周完全对称,风场均匀。因而环形板纺丝设备丝条质量的均一性相对更好。Second, the side blowing mode of the long strip spinning equipment causes the wind field contacted by the fine spinning stream at the end and the middle part of the tow belt to be uneven. The circular spinning equipment adopts circular blowing, which is completely symmetrical from the inside to the outside, and the wind field is uniform. Therefore, the uniformity of the yarn quality of the annular plate spinning equipment is relatively better.
然而,长条板纺丝设备又有很多环形板纺丝设备不具备的优势包括:However, long strip spinning equipment has many advantages that ring spinning equipment does not have, including:
第一,从设备运行性能角度来讲,长条板喷丝组件安装在保温严密的纺丝箱体中,喷丝组件的温度能够得到很好的控制,进而控制纺丝液的粘度和组件压力,有利于纺速提高。First, from the perspective of equipment operation performance, the long-strip spinneret assembly is installed in a tightly insulated spinning box, and the temperature of the spinneret assembly can be well controlled, thereby controlling the viscosity of the spinning solution and the pressure of the assembly , which is beneficial to increase the spinning speed.
第二,从操作角度上来讲,长条板纺丝设备在纺丝生头、集束,组件更换等操作上比环形板纺丝设备操作更加便捷。Second, from the perspective of operation, the operation of strip spinning equipment is more convenient than that of ring spinning equipment in terms of spinning, clustering, and component replacement.
第三,从设备加工角度来看,长条板纺丝设备的纺丝组件,吹风组件等各组件加工难度小,成本相对低。而环形板纺丝设备各组件加工精度要求高,加工难度大,进而造成设备制造成本较高。Third, from the perspective of equipment processing, the processing of the spinning components, blowing components and other components of the strip spinning equipment is less difficult and the cost is relatively low. However, each component of the ring-shaped plate spinning equipment requires high processing precision and is difficult to process, resulting in high equipment manufacturing costs.
为更进一步阐述本发明为达成预定发明目的所采取的技术手段及功效,以下结合附图及较佳实施例,对依据本发明提出的一种干喷湿纺法纺丝设备,其具体实施方式、结构、特征及其功效,详细说明如后。在下述说明中,不同的“一实施例”或“实施例”指的不一定是同一实施例。此外,一或多个实施例中的特定特征、结构、或特点可由任何合适形式组合。In order to further explain the technical means and effects of the present invention to achieve the intended purpose of the invention, the specific implementation method of a dry-jet wet spinning spinning equipment proposed according to the present invention will be described below in conjunction with the accompanying drawings and preferred embodiments. , structure, feature and effect thereof, detailed description is as follows. In the following description, different "one embodiment" or "embodiment" do not necessarily refer to the same embodiment. Furthermore, the particular features, structures, or characteristics of one or more embodiments may be combined in any suitable manner.
本文中术语“和/或”,仅仅是一种描述关联对象的关联关系,表示可以存在三种关系,例如,A和/或B,具体的理解为:可以同时包含有A与B,可以单独存在A,也可以单独存在B,能够具备上述三种任一种情况。The term "and/or" in this article is just an association relationship describing associated objects, which means that there can be three relationships, for example, A and/or B. The specific understanding is: A and B can be included at the same time, and A and B can be included separately. A exists, B may exist alone, and any of the above three situations can be met.
参见附图1-附图6,本发明提供的干喷湿纺法纺丝设备包括熔体管路3、多个喷丝组件4、冷却风管路5、凝固浴槽7、和集束导丝棒。熔体管路3包括第一种主管路和多个第一种支管路,第一种主管路与第一种支管路分别连通;第一种支管路与喷丝组件4一一对应,并且,第一种支管路与对应的喷丝组件4连通,使得经过多个喷丝组件4之后,纺丝熔体形成多组纺丝细流;冷却风管路5用于通过多向出风口向多组纺丝细流吹风;集束导丝棒设置于凝固浴槽7内,使得多组纺丝细流经过集束导丝棒后完成集束导丝。本实施例中,喷丝组件4包括两个,第一种支管路包括两个,在这种情况下,长条板纺丝设备,环形板纺丝设备与本发明实施例提供的干喷湿纺法纺丝设备的对比表如下:Referring to accompanying drawing 1-accompanying
其中,多个喷丝组件4的规格相同;多个第一种支管路规格相同。本实施例中,两个第一种支管路的口径、长度、弯头数量均完全相同,在这种情况下,能够保证每组纺丝组件4流出的纺丝细流具有较强的一致性,使得纺丝完成所得的成品丝质量均一、稳定。Among them, the specifications of the
其中,干喷湿纺法纺丝设备还包括计量泵1和计量泵箱体2。纺丝熔体经过计量泵1之后进入熔体管路3。在这种情况下,纺丝熔体经过计量后更加符合生产要求。Wherein, the dry jet wet spinning method further includes a
其中,冷却风管路5包括第二种主管路和多个第二种支管路。第二种主管路与多个第二种支管路分别连通。本实施例中,第二种支管路为两个,第二种支管的管径,弯头数量,管路长度等几何结构完全一致,在这种情况下,能够更加严格地保证分配吹风装置水平方向吹风风场均匀。干喷湿纺法纺丝设备还包括冷却风分配吹风装置6。冷却风分配吹风装置6包括腔体,腔体上设置有出风口;两个第二种支管路分别与腔体连通,两个第二种支管路在腔体上均匀布置。本实施例中,两个支管路与腔体的连接位置分别位于腔体轴向两端开始的1/4位置处,在这种情况下,能够使得经由腔体吹出的风更加均匀。Wherein, the cooling
其中,干喷湿纺法纺丝设备还包括两个挡风板9。两个挡风板9分别设置于腔体的轴向两端下方,挡风板9在水平方向的伸出长度超过纺丝流体的最远端,挡风板9的最底端处于凝固浴槽7的凝固浴液面以下。在这种情况下,在纺丝过程中,冷却风在遇到纺丝细流后,由于受到了较大的阻力,部分风因此而绕行与吹风方向垂直的水平方向,在此处与挡风板9相遇从而阻止了冷却风横向逃逸,从而在两排丝束,两个挡风板围成的方形空间内形成一个正压区,保证风场相对均匀的作用于丝束,对经过纺丝过程所得的成品丝的质量也更加有利。Wherein, the dry jet wet spinning method spinning equipment also includes two
其中,干喷湿纺法纺丝设备还包括保温夹套,保温夹套设置于熔体管路3和/或多个喷丝组件4的外围,干喷湿纺法纺丝设备还包括保温夹套,保温夹套设置于计量泵箱体2的外围。保温夹套内设置有介质腔,介质腔内充有保温介质。本实施例中,保温介质为水,通过控制水温实现温度控制。本实施例中,为了便于进行纺丝速度的调整,喷丝组件4单独设置热水保温夹套,并独立控制温度,从而适应高粘度熔体的高速纺丝。Wherein, the dry-jet wet spinning method spinning equipment also includes a thermal insulation jacket, and the thermal insulation jacket is arranged on the periphery of the
其中,干喷湿纺法纺丝设备还包括转向棒11。转向棒11设置于凝固浴槽7的出口边缘,完成集束导丝的纺丝细流经过转向棒11后完成纺丝过程。Wherein, the dry jet wet spinning method spinning equipment also includes a steering
其中,集束导丝棒包括第一集束导丝棒10,多组纺丝细流均通过第一集束导丝棒10完成集束导丝;集束导丝棒包括第多根集束导丝棒,多组纺丝细流中每组纺丝细流均至少经过一根集束导丝棒后完成集束导丝。如图2所示,集束导丝棒10为1根,纺丝细流为两个;如图5所示,集束导丝棒包括两根,分别为第二集束导丝棒12、第三集束导丝棒13,其中,第一纺丝细流经由第二集束导丝棒12集束导丝,第二纺丝细流经由第三集束导丝棒13集束导丝;如图6所示,集束导丝棒包括三根,分别为第二集束导丝棒12、第三集束导丝棒13、第四集束导丝棒14,其中,第一纺丝细流经由第二集束导丝棒12集束导丝,第二纺丝细流经由依次经由第四集束导丝棒14、第三集束导丝棒13集束导丝。其中,集束导丝棒的设置数量根据丝束对绕过集束导丝棒包角的容忍程度设置。Wherein, the clustering guide rods include the first
尽管已描述了本发明的优选实施例,但本领域内的技术人员一旦得知了基本创造性概念,则可对这些实施例作出另外的变更和修改。所以,所附权利要求意欲解释为包括优选实施例以及落入本发明范围的所有变更和修改。While preferred embodiments of the invention have been described, additional changes and modifications to these embodiments can be made by those skilled in the art once the basic inventive concept is appreciated. Therefore, it is intended that the appended claims be construed to cover the preferred embodiment as well as all changes and modifications which fall within the scope of the invention.
显然,本领域的技术人员可以对本发明进行各种改动和变型而不脱离本发明的精神和范围。这样,倘若本发明的这些修改和变型属于本发明权利要求及其等同技术的范围之内,则本发明也意图包含这些改动和变型在内。Obviously, those skilled in the art can make various changes and modifications to the present invention without departing from the spirit and scope of the present invention. Thus, if these modifications and variations of the present invention fall within the scope of the claims of the present invention and their equivalent technologies, the present invention also intends to include these modifications and variations.
Claims (11)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210092875.3A CN114277452B (en) | 2022-01-26 | 2022-01-26 | Dry-jet wet spinning spinning equipment |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210092875.3A CN114277452B (en) | 2022-01-26 | 2022-01-26 | Dry-jet wet spinning spinning equipment |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN114277452A CN114277452A (en) | 2022-04-05 |
| CN114277452B true CN114277452B (en) | 2023-01-06 |
Family
ID=80882024
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202210092875.3A Active CN114277452B (en) | 2022-01-26 | 2022-01-26 | Dry-jet wet spinning spinning equipment |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN114277452B (en) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117802591B (en) * | 2023-12-27 | 2025-10-24 | 东华大学 | A multi-in-one solidification stretching device |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN1501990A (en) * | 2001-03-14 | 2004-06-02 | ��֯�������о�Э��ͼ�ָ��о�Ժ | Method and apparatus for producing cellulosic fibers and cellulosic filament yarns |
| JP2007119973A (en) * | 2005-10-31 | 2007-05-17 | Teijin Techno Products Ltd | Dry-wet spinning apparatus and dry-wet spinning method |
| CN104928771A (en) * | 2015-06-26 | 2015-09-23 | 北京三联虹普新合纤技术服务股份有限公司 | Production process of 24 cake nylon 6 fully-drawn fibers |
| CN105350091A (en) * | 2015-11-25 | 2016-02-24 | 山东大学 | Dry-jet wet-spinning jetting device and making method thereof |
| JP2017141524A (en) * | 2016-02-10 | 2017-08-17 | 帝人株式会社 | Manufacturing method of synthetic fiber yarn |
| CN211005732U (en) * | 2019-09-10 | 2020-07-14 | 杭州中丽化纤有限公司 | A cross-air blowing slow cooling device for colored POY long filament of superfine denier |
Family Cites Families (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE10019660B4 (en) * | 2000-04-20 | 2004-04-29 | Zimmer Ag | Process for spinning a spinning solution and spinning head |
-
2022
- 2022-01-26 CN CN202210092875.3A patent/CN114277452B/en active Active
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN1501990A (en) * | 2001-03-14 | 2004-06-02 | ��֯�������о�Э��ͼ�ָ��о�Ժ | Method and apparatus for producing cellulosic fibers and cellulosic filament yarns |
| JP2007119973A (en) * | 2005-10-31 | 2007-05-17 | Teijin Techno Products Ltd | Dry-wet spinning apparatus and dry-wet spinning method |
| CN104928771A (en) * | 2015-06-26 | 2015-09-23 | 北京三联虹普新合纤技术服务股份有限公司 | Production process of 24 cake nylon 6 fully-drawn fibers |
| CN105350091A (en) * | 2015-11-25 | 2016-02-24 | 山东大学 | Dry-jet wet-spinning jetting device and making method thereof |
| JP2017141524A (en) * | 2016-02-10 | 2017-08-17 | 帝人株式会社 | Manufacturing method of synthetic fiber yarn |
| CN211005732U (en) * | 2019-09-10 | 2020-07-14 | 杭州中丽化纤有限公司 | A cross-air blowing slow cooling device for colored POY long filament of superfine denier |
Also Published As
| Publication number | Publication date |
|---|---|
| CN114277452A (en) | 2022-04-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN108642583A (en) | A kind of spinning drawing combination machine and spinning-drawing machine monomer pumping device | |
| SK284101B6 (en) | Process for manufacturing cellulose moulded bodies and a device for carrying it out | |
| CN102134759B (en) | Circular blow cooling device for producing industrial polyester filaments | |
| CN101619505A (en) | Production method of filament for capron 6 one-step full stretching superfine denier socks | |
| CN108642584B (en) | Spinning and drawing combination machine for split-fiber female yarns | |
| US20200291545A1 (en) | Device for the Extrusion of Filaments and for the Production of Spunbonded Fabrics | |
| CN104141175A (en) | Super-fine denier FDY (fully drawn yarn) spinning equipment and spinning process | |
| CN115287773B (en) | Large-tow polyimide fiber dry spinning tunnel and spinning method | |
| CN110644062A (en) | A coat-hanger-shaped spinning die runner structure for evenly distributing melt | |
| CN112981566A (en) | Spinning equipment and spinning process for semi-dull flat POY (polyester pre-oriented yarn) plied fibers | |
| CN111636125A (en) | Production method of special-shaped polyester (POY/FDY) mixed fiber composite filament | |
| US3156752A (en) | Method and apparatus for heat treating filaments | |
| CN109097848A (en) | A kind of preparation method of micro denier porous filaments flat FDY long filament | |
| JPH02145807A (en) | Method and apparatus for melting-spinning | |
| CN206635468U (en) | A kind of activated fibre spinneret | |
| CN220520703U (en) | Telescopic air return device for flash evaporation spinning | |
| CN114277452A (en) | Dry-Jet Wet Spinning Equipment | |
| CN206244954U (en) | One kind production air bag silk device for spinning | |
| CN105420824B (en) | A spinning component and spinning method thereof | |
| CN111809257A (en) | Be applied to special shower nozzle structure of nanofiber melt-blown preparation | |
| CN111719189A (en) | 5D or 7D POY spinning line equipment is blown to superfine denier veneer ring | |
| CN113957547B (en) | Production process method of multipurpose net-woven fiber raw material | |
| US1814468A (en) | Process and apparatus for the production of artificial filaments or threads | |
| US2351772A (en) | Spinning machine | |
| CN119041039A (en) | Telescopic air duct for flash evaporation spinning |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |