CN114570842B - Manufacturing and processing equipment for condenser fins for refrigeration house refrigerating system - Google Patents
Manufacturing and processing equipment for condenser fins for refrigeration house refrigerating system Download PDFInfo
- Publication number
- CN114570842B CN114570842B CN202210495797.1A CN202210495797A CN114570842B CN 114570842 B CN114570842 B CN 114570842B CN 202210495797 A CN202210495797 A CN 202210495797A CN 114570842 B CN114570842 B CN 114570842B
- Authority
- CN
- China
- Prior art keywords
- shaped
- groove
- sliding
- face
- grooves
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000005057 refrigeration Methods 0.000 title claims abstract description 23
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 16
- 238000003825 pressing Methods 0.000 claims description 17
- 230000003014 reinforcing effect Effects 0.000 claims description 7
- 238000005096 rolling process Methods 0.000 claims description 7
- 238000003860 storage Methods 0.000 claims description 7
- 230000002146 bilateral effect Effects 0.000 claims description 6
- 238000003754 machining Methods 0.000 claims 2
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 abstract description 29
- 229910052802 copper Inorganic materials 0.000 abstract description 29
- 239000010949 copper Substances 0.000 abstract description 29
- 238000003780 insertion Methods 0.000 description 7
- 230000037431 insertion Effects 0.000 description 7
- 238000000034 method Methods 0.000 description 5
- 238000006073 displacement reaction Methods 0.000 description 3
- 230000000712 assembly Effects 0.000 description 2
- 238000000429 assembly Methods 0.000 description 2
- 230000033228 biological regulation Effects 0.000 description 2
- 230000000903 blocking effect Effects 0.000 description 2
- 238000003466 welding Methods 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000001125 extrusion Methods 0.000 description 1
- 230000017525 heat dissipation Effects 0.000 description 1
- 239000007788 liquid Substances 0.000 description 1
- 230000000149 penetrating effect Effects 0.000 description 1
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D39/00—Application of procedures in order to connect objects or parts, e.g. coating with sheet metal otherwise than by plating; Tube expanders
- B21D39/06—Application of procedures in order to connect objects or parts, e.g. coating with sheet metal otherwise than by plating; Tube expanders of tubes in openings, e.g. rolling-in
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D43/00—Feeding, positioning or storing devices combined with, or arranged in, or specially adapted for use in connection with, apparatus for working or processing sheet metal, metal tubes or metal profiles; Associations therewith of cutting devices
- B21D43/003—Positioning devices
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D—WORKING OR PROCESSING OF SHEET METAL OR METAL TUBES, RODS OR PROFILES WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21D53/00—Making other particular articles
- B21D53/02—Making other particular articles heat exchangers or parts thereof, e.g. radiators, condensers fins, headers
- B21D53/06—Making other particular articles heat exchangers or parts thereof, e.g. radiators, condensers fins, headers of metal tubes
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/14—Thermal energy storage
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Automatic Assembly (AREA)
- Devices That Are Associated With Refrigeration Equipment (AREA)
Abstract
The invention relates to the technical field of condenser manufacturing, in particular to a condenser fin manufacturing and processing device for a refrigeration house refrigerating system. According to the invention, the gathering mechanism is matched with the positioning mechanism, so that the arrangement and placement of the fins are facilitated, meanwhile, the jacks among the fins can be aligned, and the copper pipes can be conveniently and rapidly inserted into the arranged fin jacks, thereby improving the assembly efficiency of the fins.
Description
Technical Field
The invention relates to the technical field of condenser manufacturing, in particular to a manufacturing and processing device for condenser fins for a refrigeration system of a refrigeration house.
Background
The condenser is a part of a refrigeration system of a refrigeration house, belongs to a heat exchanger, can convert gas or vapor into liquid, quickly transfers the heat in the tube to the air near the tube, and the fins are a heat dissipation structure of the condenser and need to be connected with copper tubes in the condenser during processing so as to be convenient for the condenser to dissipate heat quickly.
When the condenser fin is assembled and processed by adopting the prior art, the processed fins need to be arranged in sequence, and then copper pipes connected with the fins are inserted into the jacks of the fins for assembly, but the condenser fin processing mode has the following problems: 1. energy is consumed in the process of orderly arranging, placing and aligning the fins, meanwhile, jacks on the fins are prone to deviation in the aligning process, so that the jacks are difficult to align, the copper pipes are not inserted smoothly, and the assembling efficiency of the fins is reduced; 2. when carrying out fixed welding after assembling copper pipe and fin, need artifical handheld U type to link the pipe and align welding with U type copper pipe to lead to the hand labor volume to increase.
Disclosure of Invention
In order to solve the problems, the invention adopts the following technical scheme that condenser fins for a refrigeration house refrigeration system are manufactured and processed by the following equipment, the equipment comprises a processing table and adjusting frames, the adjusting frames are symmetrically arranged on the left and right sides of the upper end face of the processing table, a gathering mechanism used for limiting the fins is arranged on the adjusting frames, L-shaped push plates are arranged at the lower ends of the left adjusting frame and the right adjusting frame, the fins which are equidistantly arranged from front to back are jointly placed on the two L-shaped push plates, a sliding adjusting groove is formed in the upper end face of the processing table close to the front end, a clamping and releasing mechanism is arranged in the sliding adjusting groove through a sliding electric slider, a pushing groove is formed in the upper end face of the processing table close to the rear end, a positioning mechanism is arranged in the pushing groove through the pushing electric slider, and the pushing groove and the sliding adjusting groove are both located between the left L-shaped push plate and the right L-shaped push plate.
The clamping and releasing mechanism comprises a support plate, the upper end face of the sliding electric sliding block is provided with the support plate, the support plate is provided with waist-shaped grooves which are equidistantly distributed from top to bottom, the lower end face of each waist-shaped groove is provided with a lower pressing and receiving groove, the lower end face of each waist-shaped groove is provided with temporary placing grooves which are equidistantly distributed from left to right, the temporary placing grooves correspond to jacks on fins one by one, the temporary placing grooves are communicated with the lower pressing and receiving grooves, the left side and the right side of each waist-shaped groove are respectively provided with an L-shaped sliding groove, the vertical section of each L-shaped sliding groove penetrates through the front end face of the support plate, the lower pressing and receiving grooves are internally and slidably connected with a connecting seat, the upper end face of each connecting seat is provided with an arc seat which is uniformly distributed from left to right, the arc seats are positioned above the temporary placing grooves, the left side and the right side of each connecting seat are respectively provided with an L-shaped sliding rod, the front ends of the L-shaped sliding rods penetrate through the L-shaped sliding grooves, the corresponding to each other through a belt connecting plate, the one end that the connecting seat was kept away from to L type slide bar is installed and is pushed down electronic slider, and the lower spout that the equidistance was arranged from the top down is all seted up to the preceding terminal surface left and right sides of mounting panel, and the lower spout of the left and right sides is located respectively between two adjacent arc seats of the left and right sides, and the lower spout is linked together with pushing down the groove, and bilateral symmetry's gusset plate is installed to the preceding terminal surface of connecting seat, and the front end of gusset plate runs through and installs after the spout down and accepts the subassembly.
Preferably, accept the subassembly including placing the seat, the seat of placing of arc structure is installed to the up end of gusset plate, and the left and right sides of placing the seat is installed through the arc pole and is accepted the seat, accepts the seat and be the arc structure, and the up end position of accepting the up end of seat and arc seat is aligned.
Preferably, the upper end face of the arc seat is connected with antifriction balls which are uniformly distributed in a rolling manner.
Preferably, the positioning mechanism comprises a Y-shaped support, the upper end surface of the pushing electric slider is provided with the Y-shaped support, the front end surfaces of two vertical sections of the Y-shaped support are respectively provided with a ring-shaped seat which is arranged in an up-down symmetrical manner, the front end surface of the ring-shaped seat is connected with a fixed disc in a sliding manner, the rear end surface of the fixed disc is provided with a ring-shaped groove which is connected with the ring-shaped seat in a sliding manner, the rear end surface of the fixed disc is connected with the Y-shaped support through pushing springs which are uniformly arranged along the circumferential direction of the Y-shaped support, the front end surface of the fixed disc is provided with a retaining ring and inserting columns which are positioned in the retaining ring, the side walls of the inserting columns are provided with connecting holes which are equidistantly arranged from front to back, the connecting holes are uniformly arranged along the circumferential direction of the inserting columns, the inner walls of the front ends of the inserting columns are provided with telescopic spring rods, the rear ends of the telescopic spring rods are provided with pushing shafts which are fixedly connected with the Y-shaped support after penetrating through the fixed disc, the side walls of the pushing shafts are fixedly sleeved with pushing discs which are arranged from front to back at equal intervals, the supporting rods are connected in the connecting holes in a sliding mode, hole adjusting positioning assemblies are mounted on the supporting rods corresponding to the front and the back of the supporting rods, and the pushing disc is connected with the supporting rods through hinged push rods.
Preferably, the hole adjusting and positioning assembly is formed by rotationally connecting an Contraband-shaped frame and a supporting roller, and a supporting rod is fixedly connected with a vertical section of the Contraband-shaped frame.
Preferably, a standing plate is mounted on the rear end face of the Y-shaped support.
Preferably, the gathering mechanism includes spacing logical groove, the spacing logical groove of arranging about seting up on the alignment jig, the lower terminal surface that is located the spacing logical groove of upside offers and is linked together with the spacing logical groove that is located the downside, spacing logical inslot sliding connection has the gag lever post of arranging in the past backward equidistance, be connected through the synchronizing bar between the corresponding gag lever post from top to bottom, the synchronizing bar runs through the spread groove, the opposite face of left and right sides gag lever post all installs and keeps off the push pedal, the fin is located adjacent two and keeps off between the push pedal, be located fixed connection between the gag lever post of rear side and the spacing logical groove, the up end that is located the connecting rod of upside articulates there is the regulation pole, it is articulated mutually between two adjacent regulation poles, the preceding terminal surface that is located the gag lever post of front side installs propelling movement electronic slider.
Preferably, the storage tank has been seted up to the lower terminal surface of alignment jig, and the vertical section of L type push pedal is located the storage tank, and the finishing groove of bilateral symmetry arrangement has been seted up to the up end of processing platform, and the finishing groove is located the below of L type push pedal, and the finishing groove is connected with the lower terminal surface of L type push pedal through the electronic slider of flat push.
Preferably, a mounting groove is formed in the upper end face of the horizontal section of the L-shaped push plate, and rolling rollers are rotationally connected between the front end face and the rear end face of the mounting groove and are equidistantly arranged from left to right.
Preferably, the front end face of the baffle ring is provided with a ring-shaped rubber pad.
The invention has the beneficial effects that: 1. according to the condenser fin manufacturing and processing equipment for the refrigeration house refrigeration system, the adopted collecting and gathering mechanism is matched with the positioning mechanism, the arrangement and the placement of fins are facilitated, meanwhile, the jacks among the fins can be aligned, so that copper pipes can be conveniently and rapidly inserted into the arranged fin jacks, the assembly efficiency of the fins is improved, meanwhile, after the insertion and the placement of the U-shaped copper pipes on the fins are completed, the U-shaped connecting pipes can be placed on the clamping and placing mechanism, an operator can conveniently connect and fix the assembled fins with the U-shaped copper pipes through the U-shaped connecting pipes, and the problem that manual labor is increased due to the fact that the U-shaped connecting pipes are held by hands is solved.
2. The supporting rollers align the corresponding front and rear fin jacks through the supporting supports, so that the U-shaped copper tubes can be smoothly inserted into the jacks of the fins, the assembling efficiency of the fins is improved, and the problem of low assembling efficiency caused by multiple times of adjusting and inserting is solved.
3. The gathering mechanism can sequentially prop the fins from front to back, the fins are pushed together by the pushing of the pushing blocking plates, the problem that the fins need to be pushed one by one when being assembled is solved, and when the gathering mechanism is used, the fins only need to be placed between the pushing blocking plates which are adjacent at the front and the back of the left side and the right side, so that the fin placing efficiency is improved.
Drawings
The invention is further illustrated with reference to the following figures and examples.
Fig. 1 is a schematic view of a first three-dimensional structure of the present invention.
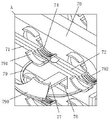
Fig. 2 is an enlarged view of fig. 1 a of the present invention.
Fig. 3 is a second perspective view of the present invention.
Fig. 4 is a top view of the present invention.
Fig. 5 is a sectional view taken along line B-B of fig. 4 in accordance with the present invention.
FIG. 6 is a top cross-sectional view of the positioning mechanism of the present invention.
Fig. 7 is an enlarged view of the invention at C of fig. 6.
FIG. 8 is a top cross-sectional view of the pinching mechanism of the present invention.
FIG. 9 is a principal direction partial sectional view of the pinching mechanism of the present invention.
FIG. 10 is a schematic view showing the structure of the fin, the U-shaped copper tube and the U-shaped connecting tube according to the present invention.
In the figure: 1. a processing table; 2. an adjusting bracket; 3. a pinching mechanism; 30. a limiting through groove; 31. a limiting rod; 32. a synchronization lever; 33. a push baffle plate; 34. adjusting a rod; 4. an L-shaped push plate; 40. a storage tank; 41. arranging a groove; 42. a rolling roller; 5. a fin; 6. a sliding adjustment groove; 7. a card placing mechanism; 70. a mounting plate; 71. a waist-shaped groove; 72. pressing down the collecting groove; 73. a connecting seat; 74. an arc-shaped seat; 75. an L-shaped sliding rod; 76. a lower chute; 77. a reinforcing plate; 78. a connecting plate; 79. a receiving assembly; 790. a placing seat; 791. a bearing seat; 792. antifriction balls; 8. a pushing groove; 9. a positioning mechanism; 90. a Y-shaped bracket; 91. an annular seat; 92. fixing the disc; 93. pushing the spring; 94. a baffle ring; 940. an annular rubber pad; 95. inserting the column; 96. a telescopic spring rod; 97. a pushing shaft; 98. pushing a disc; 99. a support rod is propped; 901. contraband form rack; 902. a roller is abutted; 910. standing the plate.
Detailed Description
Embodiments of the invention will be described in detail below with reference to the drawings, but the invention can be implemented in many different ways as defined and covered by the claims.
Refer to fig. 1, a processing equipment is made to freezer is condenser fin for refrigerating system, including processing platform 1 and alignment jig 2, bilateral symmetry's alignment jig 2 is installed to the up end of processing platform 1, install on alignment jig 2 and be used for carrying on spacing receipts gathering mechanism 3 to fin 5, control the lower extreme of two alignment jigs 2 and all install L type push pedal 4, place fin 5 that the equidistance was arranged backward in the past jointly on two L type push pedals 4, the up end of processing platform 1 is close to the front end department and has seted up sliding adjustment tank 6, install card through sliding electric slider in the sliding adjustment tank 6 and put mechanism 7, the up end of processing platform 1 is close to the rear end department and has seted up lapse groove 8, install positioning mechanism 9 through lapse electric slider in lapse groove 8, lapse groove 8 all is located between two L type push pedals 4 about with sliding adjustment tank 6.
Referring to fig. 9, storage tank 40 has been seted up to the lower terminal surface of alignment jig 2, the vertical section of L type push pedal 4 is located storage tank 40, the arrangement groove 41 that bilateral symmetry arranged is seted up to the up end of processing platform 1, arrangement groove 41 is located the below of L type push pedal 4, arrangement groove 41 is connected with the lower terminal surface of L type push pedal 4 through the electronic slider of flat push, after fin 5 placed the completion, the electronic slider of flat push drives the L type push pedal 4 of both sides to remove to fin 5, thereby align fin 5 arrangement, be convenient for the equipment in the U type copper pipe inserts the jack of fin 5.
Referring to fig. 9, a mounting groove is formed in the upper end surface of the horizontal section of the L-shaped push plate 4, rolling rollers 42 are rotatably connected between the front end surface and the rear end surface of the mounting groove and are equidistantly arranged from left to right, and the rolling rollers 42 are used for reducing the friction force between the fins 5 and the L-shaped push plate 4.
Referring to fig. 8 and 9, the gathering mechanism 3 includes a limiting through groove 30, a limiting through groove 30 arranged from top to bottom is formed in the adjusting frame 2, a connecting groove communicated with the limiting through groove 30 located on the lower side is formed in the lower end face of the limiting through groove 30 located on the upper side, limiting rods 31 arranged in the front and back at equal intervals are connected in the limiting through groove 30 in the limiting through groove, the limiting rods 31 corresponding to the upper side and the lower side are connected through synchronizing rods 32, the synchronizing rods 32 penetrate through the connecting groove, baffle push plates 33 are installed on opposite faces of the limiting rods 31 on the left side and the right side, fins 5 are located between two adjacent baffle push plates 33, the limiting rods 31 located on the rear side and the limiting through groove 30 are fixedly connected, adjusting rods 34 are hinged to the upper end face of the connecting rod located on the upper side, two adjacent adjusting rods 34 are hinged to each other, and an electric pushing sliding block is installed on the front end face of the limiting rods 31 located on the front side.
Referring to fig. 6 and 7, the positioning mechanism 9 includes a Y-shaped support 90, the upper end surface of the pushing electric slider is provided with the Y-shaped support 90, the front end surfaces of two vertical sections of the Y-shaped support 90 are respectively provided with an annular seat 91 which is arranged vertically and symmetrically, the front end surface of the annular seat 91 is connected with a fixed disk 92 in a sliding manner, the rear end surface of the fixed disk 92 is provided with an annular groove which is connected with the annular seat 91 in a sliding manner, the rear end surface of the fixed disk 92 is connected with the Y-shaped support 90 through pushing springs 93 which are uniformly arranged along the circumferential direction of the Y-shaped support, the front end surface of the fixed disk 92 is provided with a retaining ring 94 and an inserting column 95, the inserting column 95 is positioned in the retaining ring 94, the side wall of the inserting column 95 is provided with connecting holes which are equidistantly arranged from front to back, the connecting holes are uniformly arranged along the circumferential direction of the inserting column 95, the front end inner wall of the inserting column 95 is provided with a telescopic spring rod 96, the rear end of the telescopic spring rod 96 is provided with a pushing shaft 97, the rear end of the pushing shaft 97 penetrates through the fixed disc 92 and then is fixedly connected with the Y-shaped support 90, the side wall of the pushing shaft 97 is fixedly sleeved with pushing discs 98 which are arranged from front to back at equal intervals, supporting rods 99 are connected in the connecting holes in a sliding mode, hole adjusting positioning assemblies are mounted on the supporting rods 99 which correspond to each other in the front and back, and the pushing discs 98 are connected with the supporting rods 99 through hinged push rods.
Referring to fig. 7, the hole adjusting positioning assembly is formed by rotatably connecting a v-shaped frame 21274with a resisting roller 902, and the vertical sections of the v-shaped frame 901 are fixedly connected with a resisting stay bar 99 and the v-shaped frame 21274.
The Y-shaped support 90 is pushed to move forwards by pushing the electric sliding block, so that the inserting and placing column 95 is inserted into the jack of the fin 5, when the baffle ring 94 is abutted against the fin 5 on the rear side, the Y-shaped support 90 extrudes the extruding and pushing spring 93 to enable the annular seat 91 to move towards the annular groove, meanwhile, the Y-shaped support 90 pushes the pushing shaft 97 connected with the Y-shaped support to move forwards and extrudes the telescopic spring rod 96 to contract, meanwhile, the pushing shaft 97 drives the pushing disc 98 to move forwards, the pushing rod and the abutting rod 99 push the Contraband-shaped frame 901 to be opened in the process that the pushing disc 98 moves forwards until the abutting roller 902 is abutted against the inner wall of the jack of the fin 5, the corresponding front and rear jacks of the fin 5 are aligned through the abutting support of the abutting roller 902, so that a U-shaped copper tube can be smoothly inserted into the jack of the fin 5, the assembly efficiency of the fin 5 is improved, the problem of low assembly efficiency caused by multiple times of adjustment and insertion is avoided, and meanwhile, the abutting roller 902 is contacted with the jack of the fin 5, thereby reduce the area of contact between jack and the roller 902 that supports, the difficult dead phenomenon of card that appears is convenient for adjust fin 5.
Referring to fig. 6, a ring-shaped rubber pad 940 is mounted on the front end surface of the baffle ring 94, and the ring-shaped rubber pad 940 is used for reducing the extrusion damage force of the baffle ring 94 on the side wall of the fin 5.
Referring to fig. 1, 2, 4 and 5, the locking and releasing mechanism 7 includes a support plate 70, the support plate 70 is installed on the upper end surface of the sliding electric slider, waist-shaped grooves 71 are formed on the support plate 70 and are equidistantly arranged from top to bottom, lower end surfaces of the waist-shaped grooves 71 are formed with lower pressing and retracting grooves 72, lower end surfaces of the waist-shaped grooves 71 are formed with temporary placing grooves which are equidistantly arranged from left to right, the temporary placing grooves correspond to insertion holes on the fins 5 one by one, the temporary placing grooves are communicated with the lower pressing and retracting grooves 72, L-shaped sliding grooves are formed on the left and right sides of the waist-shaped grooves 71, vertical sections of the L-shaped sliding grooves penetrate through the front end surface of the support plate 70, connecting seats 73 are slidably connected in the lower pressing and retracting grooves 72, arc-shaped seats 74 are uniformly arranged from left to right on the upper end surface of the connecting seats 73, the arc-shaped seats 74 are located above the temporary placing grooves, L-shaped sliding rods 75 are installed on the left and right sides of the connecting seats 73, the front ends of the L-shaped sliding rods 75 penetrate through the L-shaped sliding grooves, the upper and lower corresponding L-shaped sliding rods 75 are connected through a connecting plate 78, one end of each L-shaped sliding rod 75, which is far away from the connecting seat 73, is provided with a downward-pressing electric slider, the left and right sides of the front end surface of the support plate 70 are provided with downward sliding grooves 76 which are equidistantly arranged from top to bottom, the downward sliding grooves 76 of the left and right sides are respectively positioned between two adjacent arc-shaped seats 74 of the left and right sides, the downward sliding grooves 76 are communicated with the downward pressing grooves 72, the front end surface of the connecting seat 73 is provided with reinforcing plates 77 which are symmetrically arranged from left to right, and the front ends of the reinforcing plates 77 penetrate through the downward sliding grooves 76 and are provided with bearing components 79.
Referring to fig. 2 and 10, the receiving assembly 79 includes a placing seat 790, the placing seat 790 having an arc structure is mounted on the upper end surface of the reinforcing plate 77, receiving seats 791 are mounted on the left and right sides of the placing seat 790 through arc rods, the receiving seats 791 have an arc structure, and the upper end surface of the receiving seat 791 is aligned with the upper end surface of the arc seat 74.
The front ends of two vertical sections of the U-shaped copper pipe penetrate through the jacks of the fins 5 and then are placed on the arc-shaped seat 74, the arc-shaped seat 74 supports the front ends of the U-shaped copper pipe, after the U-shaped copper pipe is completely inserted into the jacks of the fins 5, the U-shaped connecting pipes are sequentially placed on the placing seat 790, the two vertical sections of the U-shaped connecting pipes are supported by the bearing seats 791 on the two sides of the placing seat 790, after the U-shaped connecting pipes are placed, the U-shaped connecting pipes are aligned with the front sides of the U-shaped copper pipe, so that the front ends of the U-shaped copper pipe and the U-shaped connecting pipes are fixedly welded, the problem that manual labor amount is increased by holding the U-shaped connecting pipes is solved, after the front ends of the U-shaped copper pipe and the U-shaped connecting pipes are fixedly welded, the pressing electric sliding block is started, the pressing electric sliding block pushes the L-shaped sliding rod 75 connected with the pressing electric sliding block to move downwards synchronously with the connecting seat 73, and simultaneously the L-shaped sliding rod 75 pushes the connecting seat 73 on the lower side under the connecting action of the connecting plate 78 to move downwards synchronously, the connecting seat 73 drives the arc-shaped seat 74 and the bearing seat 791 to move downwards in the downward moving process, so that the bearing seat 791, the placing seat 790 and the arc-shaped seat 74 no longer support the fixed U-shaped copper tube, and then the bracket plate 70 moves forwards, so that the condenser fin 5 and the copper tube after being connected, assembled and fixed can be taken out conveniently.
Referring to fig. 2, the arc-shaped upper end surface of the arc-shaped seat 74 is connected with antifriction balls 792 which are evenly arranged in a rolling manner, and the antifriction balls 792 are used for reducing the friction force between the U-shaped copper pipe and the arc-shaped seat 74.
Referring to fig. 3, a standing plate 910 is mounted on the rear end surface of the Y-shaped support 90, and the standing plate 910 is convenient for an operator to stand on the upper end thereof to insert the U-shaped copper pipe into the insertion hole of the fin 5.
When the condenser fin 5 is in specific work, the fins 5 are sequentially placed between the left L-shaped push plate 4 and the right L-shaped push plate 4, after the fins 5 are completely placed, the left side and the right side of each fin 5 are pushed by the left L-shaped push plate 4 and the right L-shaped push plate 4, the fins 5 are arranged, then the fins 5 are completely pushed backwards by the gathering mechanism 3 until the two adjacent fins 5 are tightly abutted, then the pushing electric slide block is started, the positioning mechanism 9 is driven to move forwards by the pushing electric slide block, the inserting and placing columns 95 on the positioning mechanism 9 are inserted into the inserting holes at the four corners of the fins 5, and the inserting holes of the fins 5 are uniformly supported from inside, so that the inserting holes on the front fins 5 and the rear fins 5 are completely aligned, copper pipes are rapidly and accurately inserted into the inserting holes, the assembling efficiency of the condenser fins 5 is improved, then the clamping and placing mechanism 7 is pushed backwards by the sliding electric slide block until the clamping and placing mechanism 7 is tightly attached to the fins 5 on the front side, then, a copper pipe of a U-shaped structure is inserted into the rear side of the fin 5, the U-shaped copper pipe is inserted into the left and right adjacent insertion holes in the middle of the fin 5, so that the position of the fin 5 is limited, then the electric sliding block is pushed to drive the positioning mechanism 9 to move backwards, the inserting and placing column 95 is taken out of the insertion holes of the fin 5, another copper pipe of another U-shaped structure is inserted into another two adjacent insertion holes of the fin 5, and finally, a U-shaped connecting pipe connected with the U-shaped copper pipe is placed on the clamping and placing mechanism 7, so that the U-shaped copper pipe is fixedly connected with the U-shaped connecting pipe.
Furthermore, it should be understood that although the present description refers to embodiments, not every embodiment may contain only a single embodiment, and such description is for clarity only, and those skilled in the art should integrate the description, and the embodiments may be combined as appropriate to form other embodiments understood by those skilled in the art.
Claims (10)
1. The utility model provides a processing equipment is made to freezer is condenser fin for refrigerating system, includes processing platform (1) and alignment jig (2), alignment jig (2) that bilateral symmetry arranged, its characterized in that are installed to the up end of processing platform (1): the fin fixing device is characterized in that a gathering mechanism (3) for limiting fins (5) is mounted on each adjusting frame (2), L-shaped push plates (4) are mounted at the lower ends of the left adjusting frame and the right adjusting frame (2), fins (5) which are arranged from front to back at equal intervals are commonly placed on the two L-shaped push plates (4), a sliding adjusting groove (6) is formed in the upper end face of the machining table (1) close to the front end, a clamping and releasing mechanism (7) is mounted in the sliding adjusting groove (6) through a sliding electric slider, a pushing groove (8) is formed in the upper end face of the machining table (1) close to the rear end, a positioning mechanism (9) is mounted in the pushing groove (8) through a pushing electric slider, and the pushing groove (8) and the sliding adjusting groove (6) are located between the left L-shaped push plate and the right L-shaped push plate (4);
the clamping and releasing mechanism (7) comprises a support plate (70), the support plate (70) is installed on the upper end face of the sliding electric sliding block, waist-shaped grooves (71) which are equidistantly distributed from top to bottom are formed in the support plate (70), lower end faces of the waist-shaped grooves (71) are provided with lower pressing and retracting grooves (72), temporary placing grooves which are equidistantly distributed from left to right are formed in the lower end faces of the waist-shaped grooves (71), the temporary placing grooves correspond to jacks on fins (5) one by one, the temporary placing grooves are communicated with the lower pressing and retracting grooves (72), L-shaped sliding grooves are formed in the left side and the right side of each waist-shaped groove (71), vertical sections of the L-shaped sliding grooves penetrate through the front end face of the support plate (70), connecting seats (73) are connected in the lower pressing and retracting grooves (72) in a sliding mode, arc-shaped seats (74) which are uniformly distributed from right are installed on the upper end face of each connecting seat (73), the arc-shaped seats (74) are located above the temporary placing grooves, L-shaped sliding rods (75) are installed on the left side and right side of each connecting seat (73), the front end of the L-shaped sliding rod (75) penetrates through the L-shaped sliding groove, the L-shaped sliding rods (75) corresponding to each other in the vertical direction are connected through a connecting plate (78), one end, far away from the connecting seat (73), of each L-shaped sliding rod (75) is provided with a downward-pressing electric slider, the left side and the right side of the front end face of the support plate (70) are provided with lower sliding grooves (76) which are distributed equidistantly from top to bottom, the lower sliding grooves (76) in the left side and the right side are respectively located between two adjacent arc-shaped seats (74) in the left side and the right side, the lower sliding grooves (76) are communicated with the lower pressing groove (72), reinforcing plates (77) which are symmetrically distributed in the left side and the right side are installed on the front end face of the connecting seat (73), and a bearing assembly (79) is installed after the front ends of the reinforcing plates (77) penetrate through the lower sliding grooves (76).
2. The manufacturing and processing equipment of the condenser fin for the refrigeration house refrigerating system according to claim 1, characterized in that: the supporting assembly (79) comprises a supporting seat (790), the upper end face of the reinforcing plate (77) is provided with a supporting seat (790) with an arc structure, the left side and the right side of the supporting seat (790) are provided with supporting seats (791) through arc-shaped rods, the supporting seats (791) are of arc structures, and the upper end faces of the supporting seats (791) are aligned to the upper end face of the arc-shaped seat (74).
3. The manufacturing and processing equipment of the condenser fin for the refrigeration house refrigerating system according to claim 1, characterized in that: the arc-shaped upper end surface of the arc-shaped seat (74) is in rolling connection with antifriction balls (792) which are uniformly distributed.
4. The manufacturing and processing equipment of the condenser fin for the refrigeration house refrigeration system according to claim 1, characterized in that: the positioning mechanism (9) comprises a Y-shaped support (90), the Y-shaped support (90) is installed on the upper end face of the pushing electric sliding block, ring-shaped seats (91) which are vertically and symmetrically arranged are installed on the front end faces of two vertical sections of the Y-shaped support (90), a fixing disc (92) is connected to the front end face of each ring-shaped seat (91) in a sliding mode, a ring-shaped groove which is connected with each ring-shaped seat (91) in a sliding mode is formed in the rear end face of each fixing disc (92), the rear end face of each fixing disc (92) is connected with the Y-shaped support (90) through squeezing springs (93) which are evenly distributed along the circumferential direction of the fixing disc, retaining rings (94) and inserting columns (95) are installed on the front end face of each fixing disc (92), the inserting columns (95) are located in the retaining rings (94), connecting holes which are evenly distributed from front to rear at equal intervals are formed in the side walls of the inserting columns (95), the connecting holes are evenly distributed along the circumferential direction of the inserting columns (95), telescopic spring rods (96) are installed on the inner walls of the front ends of the inserting columns (95), propelling movement axle (97) are installed to the rear end of telescopic spring pole (96), the rear end of propelling movement axle (97) runs through fixed disk (92) back and Y type support (90) fixed connection, the fixed cover of lateral wall of propelling movement axle (97) is equipped with in the past backward equidistance push away dish (98) of arranging, sliding connection has in the connecting hole and supports vaulting pole (99), front and back corresponding support install jointly on vaulting pole (99) and transfer hole locating component, push away dish (98) and support and be connected through the articulated push rod between vaulting pole (99).
5. The manufacturing and processing equipment of the condenser fin for the refrigeration house refrigeration system according to claim 4, characterized in that: the hole adjusting positioning component is formed by rotationally connecting an Contraband-shaped frame (901) and a resisting roller (902), and a resisting support rod (99) is fixedly connected with a vertical section of the V-shaped frame (901).
6. The manufacturing and processing equipment of the condenser fin for the refrigeration house refrigeration system according to claim 4, characterized in that: and a standing plate (910) is arranged on the rear end surface of the Y-shaped support (90).
7. The manufacturing and processing equipment of the condenser fin for the refrigeration house refrigerating system according to claim 1, characterized in that: the gathering mechanism (3) comprises a limiting through groove (30), the adjusting frame (2) is provided with a limiting through groove (30) which is vertically arranged, the lower end face of the limiting through groove (30) positioned on the upper side is provided with a connecting groove communicated with the limiting through groove (30) positioned on the lower side, the limiting through groove (30) is internally and slidably connected with limiting rods (31) which are equidistantly arranged from front to back, the limiting rods (31) which are corresponding to each other up and down are connected through a synchronizing rod (32), the synchronizing rod (32) penetrates through the connecting groove, the opposite faces of the limiting rods (31) on the left side and the right side are respectively provided with a baffle push plate (33), the fin (5) is positioned between two adjacent baffle push plates (33), the limiting rod (31) positioned on the rear side is fixedly connected with the limiting through groove (30), the upper end face of the connecting rod positioned on the upper side is hinged with an adjusting rod (34), and the two adjacent adjusting rods (34) are hinged with each other, the front end face of a limiting rod (31) positioned on the front side is provided with an electric pushing sliding block.
8. The manufacturing and processing equipment of the condenser fin for the refrigeration house refrigerating system according to claim 1, characterized in that: storage tank (40) have been seted up to the lower terminal surface of alignment jig (2), and the vertical section of L type push pedal (4) is located storage tank (40), and processing platform (1) upper end surface is seted up bilateral symmetry and is arranged arrangement groove (41), and arrangement groove (41) are located the below of L type push pedal (4), and arrangement groove (41) are connected with the lower terminal surface of L type push pedal (4) through the electronic slider of flat push.
9. The manufacturing and processing equipment of the condenser fin for the refrigeration house refrigerating system according to claim 1, characterized in that: the mounting groove has been seted up to the horizontal segment up end of L type push pedal (4), rotates between the front and back both ends face of mounting groove to be connected with from the roll roller (42) that the left hand right equidistance was arranged.
10. The manufacturing and processing equipment of the condenser fin for the refrigeration house refrigerating system according to claim 4, characterized in that: and a ring-shaped rubber pad (940) is arranged on the front end surface of the baffle ring (94).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210495797.1A CN114570842B (en) | 2022-05-09 | 2022-05-09 | Manufacturing and processing equipment for condenser fins for refrigeration house refrigerating system |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210495797.1A CN114570842B (en) | 2022-05-09 | 2022-05-09 | Manufacturing and processing equipment for condenser fins for refrigeration house refrigerating system |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN114570842A CN114570842A (en) | 2022-06-03 |
| CN114570842B true CN114570842B (en) | 2022-07-22 |
Family
ID=81767660
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202210495797.1A Active CN114570842B (en) | 2022-05-09 | 2022-05-09 | Manufacturing and processing equipment for condenser fins for refrigeration house refrigerating system |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN114570842B (en) |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS6099532A (en) * | 1983-10-31 | 1985-06-03 | Matsushita Electric Ind Co Ltd | Fin insertion device |
| CN202804580U (en) * | 2012-08-17 | 2013-03-20 | 中山市奥美森工业有限公司 | A fully automatic pipe threading device for inserting copper pipes into condenser fins |
| CN203993007U (en) * | 2014-08-27 | 2014-12-10 | 山东大学 | A kind of air-conditioning condenser and evaporator fin automatic intubation machine |
| CN105171368B (en) * | 2015-09-01 | 2019-04-30 | 徐州德坤电气科技有限公司 | A kind of fin is always grown up U-tube automatic intubation system and its application method |
| CN112894293B (en) * | 2019-12-03 | 2024-07-23 | 宁波远东汽车部件制造有限公司 | Radiating tube fin inserting device |
-
2022
- 2022-05-09 CN CN202210495797.1A patent/CN114570842B/en active Active
Also Published As
| Publication number | Publication date |
|---|---|
| CN114570842A (en) | 2022-06-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN118081159B (en) | Welding positioning device with force limiting function for welded plate type heat exchanger | |
| CN117644308B (en) | Auxiliary welding device for gas pipeline | |
| CN118635858B (en) | Heat exchanger installation equipment | |
| CN114570842A (en) | Manufacturing and processing equipment for condenser fins for refrigeration house refrigerating system | |
| CN113649759B (en) | A steel structure manufacturing, processing, clamping and assembling device | |
| CN114734169B (en) | Automatic welding equipment and process for radiating pipe | |
| CN111730327A (en) | Power battery cooling pipe tail end double-head assembling machine | |
| CN214898357U (en) | 13-groove insert storage tool | |
| CN119238413B (en) | Automatic assembly equipment for geothermal energy air duct | |
| CN118162879B (en) | Assembling device for radiating fin and using method thereof | |
| CN118926718A (en) | Laser cutting equipment and method for processing infrared heating tubes | |
| CN115026484B (en) | Solar street lamp pole welding equipment | |
| CN115615159B (en) | Grinding wheel drying equipment with high space utilization rate and drying method | |
| CN115771585A (en) | A waterproof hub positioning and assembly equipment and process | |
| CN212886133U (en) | Power battery cooling pipe tail end double-head assembling machine | |
| CN212886086U (en) | Tail end connector assembly machine of power battery cooling pipe | |
| CN210281289U (en) | Heat exchanger collecting pipe assembly | |
| CN114012428A (en) | Computer host base assembling device | |
| CN119772041B (en) | Fin processing device and fin processing method | |
| CN114524166A (en) | Combined type plugboard frame for processing circuit board | |
| CN116921975B (en) | Fixing clamp and method for welding shell and tube cooler | |
| CN220850428U (en) | Guide shaft support convenient to adjust | |
| CN120286790B (en) | A heat exchanger pipe tapping mechanism | |
| CN220974701U (en) | U-shaped pipe packing device of photovoltaic support | |
| CN219805636U (en) | Adjustable clamp for welding steel pipes |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |