High-efficient thick liquid greasy dirt piece-rate system
Technical Field
The utility model relates to a flue gas desulfurization technical field, concretely relates to high-efficient thick liquid greasy dirt piece-rate system.
Background
With the rapid development of social economy in China, industrial kilns, power plant boilers and the like are built in large quantities, and industrial flue gas generated by the industrial kilns contains SO2、NOxHarmful substances such as HCl, HF, dust and the like can cause environmental problems such as acid rain, corrosion of buildings and the like if not controlled, and also have the problem of harming human health.
The requirement of the national government and the public society on environmental protection is continuously improved, and particularly, the SO in the industrial flue gas is generated since the implementation of the national ultra-low emission policy in 20142、NOxAnd dust and other harmful substances are widely treated, and a high-efficiency limestone gypsum wet flue gas desulfurization technology is mostly adopted, so that the large emission reduction of related pollutants is realized. However, asphalt smoke generated by an industrial roasting furnace, oil smoke generated in the oil feeding stage of a coal-fired power plant and the like contain a large amount of tar components, other oil stain components and the like. The oil stains can be washed by the desulfurization absorption tower and enter a desulfurization slurry system, so that a plurality of adverse conditions are generated, mainly:
(1) the scale is attached and scaled on the tower wall, the pipe wall, the inner wall of the nozzle, the inner surface of the equipment and the like, so that the blockage is caused, particularly at the filter screen;
(2) wrapping the absorbent to poison the slurry in the absorption tower, so that the flue gas desulfurization reaction cannot be carried out;
(3) the tar has complex components, has certain decomposition effect on materials such as anticorrosive rubber and the like, and can cause serious system corrosion;
(4) the oil stain can prevent the gypsum from dehydrating and is mixed into the gypsum, so that the oil-containing dirty gypsum cannot be comprehensively utilized, and the tar is dangerous waste according to the relevant national regulations, so the oil stain can only be landfilled.
From the above problems, it can be seen that if the oil contamination is not separated, the oil contamination directly enters the desulfurization equipment, which has a great influence on the oil contamination, the service life of the desulfurization absorption tower and other related equipment can be obviously shortened, and certain safety accidents can be caused seriously, so that an efficient slurry oil contamination separation technology is urgently required in the industry.
SUMMERY OF THE UTILITY MODEL
In order to overcome the defect of above-mentioned prior art, the utility model provides a high-efficient thick liquid greasy dirt piece-rate system utilizes desulfurization process condition, and through the density difference of the different states of medium, the effective separation of realization greasy dirt and desulfurization thick liquid to guarantee desulfurization thick liquid system normal operating, improve the gypsum quality so that comprehensive utilization etc..
The technical scheme of the utility model as follows:
the utility model provides a high-efficient thick liquid greasy dirt piece-rate system which characterized in that: mainly comprises a light oil dirt separation device for separating oil dirt-containing slurry discharged from the upper part of a desulfurization absorption tower and a heavy oil dirt separation device for separating mixed heavy oil dirt-containing slurry;
the inside of the light oil-sewage separation device is divided into a bubbling separation area, an oil storage tank and a slurry buffer area, the bubbling separation area is communicated with the top space of the oil storage tank, and the bubbling separation area is communicated with the bottom space of the slurry buffer area; the top of the bubbling separation zone is provided with an oily sludge liquid inlet and a first slurry circulating inlet, the oily sludge liquid inlet is connected with an oily sludge liquid outlet at the upper part of the desulfurization absorption tower through a pipeline, and a bubbling pipe network is arranged in a downward area in the bubbling separation zone; the lower part of the wall of the oil storage pool is provided with a first oil stain outlet and a first slurry outlet, and the first slurry outlet is connected to a first slurry circulating inlet at the top of the bubbling separation area through a pipeline; a second slurry outlet is formed in the lower portion of the pool wall of the slurry buffer area, the second slurry outlet is externally connected with three pipelines, the first pipeline is connected to a second slurry circulation inlet in the top of the slurry buffer area to form a slurry circulation loop, the second pipeline is connected to a desulfurization absorption tower to form a slurry loop spray pipe loop, and the third pipeline is connected to a heavy oil sludge separation device to form a heavy oil sludge slurry pipeline;
the top of heavy oil dirt separator is provided with the first import of the filtrating and the overflow that flow into gypsum dewatering system, and the bottom is provided with greasy dirt export, and the middle part of lateral wall is provided with the second import that flows into light oil dirt separator discharge thick liquid and the third import that flows into desulfurization absorption tower thick liquid bottom of the pool, and the lateral wall still is provided with the thick liquid discharge port that is higher than second import and third import, and the thick liquid discharge port passes through the pipeline and can be connected to desulfurization absorption tower region drain pit.
On the basis of the basic structure, the following structure design can be made:
the bubbling separation area can be designed into a multi-time separation structure, the tops of the multi-time separation areas are communicated, and the heights of the partition plates between the two separation areas are gradually reduced to form a slurry enrichment flow direction. For example, the device is designed to comprise a primary separation area and a secondary separation area, wherein the primary separation area is communicated with the top of the secondary separation area, a partition plate between the primary separation area and the secondary separation area is higher than a partition plate between the secondary separation area and an oil storage tank, so that the operating liquid level of the secondary separation area is convenient to control, and light oil dirt can be enriched to the partition plate between the secondary separation area and the oil storage tank under the horizontal pushing action after overflow liquid falls down.
And the bottoms of the secondary and the last separation zones are provided with third slurry discharge ports, and the third slurry discharge ports are connected to the first slurry circulating inlet at the top of the bubbling separation zone through pipelines.
And a communicating hole for slurry circulation is reserved between the bottom end of the partition plate between the bubbling separation area and the slurry buffer area and the bottom plate of the light oil sewage separation device, so that the slurry flows conveniently, and the slurry liquid level of the bubbling separation area is maintained.
The bubbling pipe network is close to the position of the communicating hole, but is higher than the highest position of the communicating hole.
The specific height of the communicating holes and the height of the bubbling pipe network are specifically set according to the overall design structure size of the equipment and other relevant factors.
Furthermore, a first stirring device is arranged in the slurry buffer area and used for stirring and mixing the separated slurry at different moments, so that the slurry is uniformly mixed, and the density is consistent.
Furthermore, on the structural design of the heavy oil dirt separation device, the whole heavy oil dirt separation device comprises a cylindrical mixing area positioned on the upper part and a funnel-shaped sinking area positioned on the lower part, and a second stirring device is arranged in the mixing area and used for stirring and mixing heavy oil-containing slurry entering from different inlets, so that the heavy oil-containing slurry is uniformly mixed, and the density is consistent.
For the design on the pipeline, the following further design can be made:
the first slurry outlet is connected to a pipeline of the first slurry circulating inlet, a recirculating pump is arranged on the pipeline, and slurry discharged from the oil storage tank is pumped into the first slurry circulating inlet through the recirculating pump; when a multi-separation structure is designed, the third slurry outlet is connected to the front end of the recirculation pump, and slurry discharged from the oil storage tank and slurry in the secondary separation area and the subsequent separation area are pumped into the first slurry circulation inlet through the recirculation pump.
And the outside of the second slurry outlet is connected with the three pipelines through a slurry return pump.
And a third inlet of the heavy oil dirt separation device is provided with a slurry sewage pump on an external inflow pipeline, and the slurry sewage pump is used for pumping slurry at the bottom of the slurry pool of the desulfurization absorption tower into the heavy oil dirt separation device.
The utility model discloses an overall working principle as follows:
in the field, in actual operation, when the oil contamination is higher than 1%, the desulfurization reaction is adversely affected, the gypsum quality is poor, droplets of the flue gas which is just washed are arranged at the upper part of a slurry pool of a desulfurization absorption tower, the oil content is higher and can often reach more than 3%. Therefore, through the utility model discloses can realize handling this part greasy dirt thick liquid. The oil-containing slurry on the upper part of the slurry pool of the desulfurization absorption tower flows into the light oil separation device through the oil-containing slurry inlet, the bubbling separation is carried out through the bubbling separation area, the light oil stain overflows from the top of the bubbling separation area and enters the oil storage pool, the light oil stain in the oil storage pool is directly discharged outside for treatment, the oil-containing slurry at the bottom of the oil storage pool circulates back to the bubbling separation area again for separation, and the heavy oil-containing slurry precipitated at the bottom of the bubbling separation area continuously enters the slurry buffer area through the bottom connecting through hole. Therefore, the light oil separation device can fully utilize the high density of the slurry to separate the light oil dirt and the slurry by means of air-blowing separation and recycling. Then, the part of slurry is returned to the spraying absorption tower through a slurry return pump or injected into a heavy oil separation device, meanwhile, thick slurry at the bottom of a slurry pool of the desulfurization absorption tower is also sent to the heavy oil separation device through a slurry pool sewage discharge pump, in addition, overflow and filtrate of a gypsum dehydration system are also injected into the heavy oil separation device, and the heavy oil pollution and the slurry are separated by utilizing the reduction of the density of the slurry in the heavy oil separation device.
The utility model discloses the technique has following advantage and beneficial effect:
(1) by adjusting the density of the slurry containing oil stains and matching with mechanical separation equipment, the input of materials is not increased, and the separation of light oil stains and heavy oil stains can be easily realized.
(2) This system is external auxiliary assembly, need not to reform transform current equipment by a wide margin under the prerequisite, only reforms transform a small amount of interfaces and pipe-line system to the density of adjustment oil-containing slurry, and then realize the separation of greasy dirt, improve desulfurization slurry quality, guarantee system normal operating and gypsum quality etc. sparingly reform transform expense and time limit for a project simultaneously.
(3) The system fully utilizes the prior oxidation air system, the gypsum dewatering system, the slurry recovery system and the like on the premise of not influencing the normal operation of the prior desulfurization system, only sets of two sets of separation devices, auxiliary pumps, pipelines and the like are arranged, the system is simple and easy, the occupied area is small, the power consumption is low, and the system can be arranged nearby a desulfurization absorption tower.
(4) The separated oil stain has high heat value, can be recycled for combustion and utilization, and does not cause secondary pollution to the environment.
(5) According to the actual separation, the separated oil stain contains about 5% of inorganic salt and has the water content of about 50%, so that harmful substances such as inert particulate substances, heavy metal components, Cl ions, F ions and the like are discharged along with the oil stain discharge, the slurry quality is favorably improved, the efficient operation of a desulfurization system is ensured, and the operation pressure of a desulfurization wastewater treatment system is reduced.
(6) The system has simple equipment and is convenient to clean, and the waste liquid enters the slurry recovery system for recycling, thereby not causing secondary pollution to the environment; the system equipment is basically the same as the existing slurry tank pump of the desulfurization system, is convenient to operate and maintain, and can not increase the working difficulty.
To sum up, the utility model discloses overall structure design is simple, and the operation is maintained conveniently, can realize the separation of greasy dirt effectively, improves the desulfurization thick liquid quality, guarantees desulfurization system normal operating and gypsum quality, reduces the operation degree of difficulty, and then reduces desulfurization system and synthesizes the operation cost.
Drawings
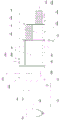
Fig. 1 is the structure schematic diagram of the light oil contamination separation system of the present invention.
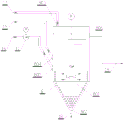
Fig. 2 is the structure schematic diagram of the heavy oil dirt separation system of the utility model.
Wherein the reference numerals are: 1 primary separation area, 101 primary separation baffle, 102 oil-containing slurry inlet, 103 first slurry circulation inlet, 2 secondary separation area, 201 secondary separation baffle, 202 third slurry outlet, 3 oil reservoir, 301 first slurry outlet, 302 first oil stain outlet, 4 slurry buffer area, 401 second slurry outlet, 402 second slurry circulation inlet, 5 bubbling pipe network, 6 communication hole, 7 first stirring device, 8 heavy oil stain separation device, 801 second stirring device, 802 oil stain outlet, 803 first inlet, 804 second inlet, 805 third inlet, 806 slurry outlet, 9 recirculation pump, 10 slurry return pump, 11 slurry blow-down pump, 12 oil-containing slurry on the upper part of absorption tower slurry, 13 high-concentration light oil stain, 14 back-spraying desulfurization absorption tower slurry, 15 light oil stain separation device discharge slurry, 16 desulfurization tower slurry at the bottom of the slurry pool, 17 filtrate and overflow of the gypsum dehydration system, 18 high-concentration heavy oil stains and 19 slurry to a drainage pit in the absorption tower area of the desulfurization tower.
Detailed Description
The present invention will be described in further detail below with reference to fig. 1 and 2 and the following examples, but the embodiments of the present invention are not limited thereto.
Example 1
A high-efficiency slurry oil stain separation system mainly comprises a light oil stain separation device and a heavy oil stain separation device, wherein the light oil stain separation device is used for separating oil-containing slurry 12 discharged from the upper part of a desulfurization absorption tower, and the heavy oil stain separation device is used for separating and mixing the heavy oil-containing slurry 8.
As shown in fig. 1, the inside of the light oil pollution separation device is divided into a bubbling separation zone, an oil storage tank 3 and a slurry buffer zone 4. Wherein: the bubbling separation zone is communicated with the top space of the oil storage tank 3, and the bubbling separation zone is communicated with the bottom space of the slurry buffer zone 4; the top of the bubbling separation zone is provided with an oily sludge slurry inlet 102 and a first slurry circulating inlet 103, the oily sludge slurry inlet 102 is connected with an oily sludge outlet at the upper part of the desulfurization absorption tower through a pipeline, and a bubbling pipe network 5 is arranged in a downward area in the bubbling separation zone; a first oil stain outlet 302 and a first slurry outlet 301 are arranged at the lower part of the wall of the oil storage tank 3, and the first slurry outlet 301 is connected to a first slurry circulating inlet 103 at the top of the bubbling separation zone through a pipeline; a second slurry outlet 401 is arranged at the lower part of the pool wall of the slurry buffer area 4, the second slurry outlet 401 is externally connected with three pipelines, the first pipeline is connected to a second slurry circulation inlet 402 at the top of the slurry buffer area 4 to form a slurry circulation loop, the second pipeline is connected to a desulfurization absorption tower to form a slurry loop spraying pipeline, and the third pipeline is connected to the heavy oil pollution separation device 8 to form a heavy oil pollution slurry pipeline.
As shown in fig. 2, the top of the heavy oil-sewage separation device 8 is provided with a first inlet 803 for filtrate and overflow flowing into the gypsum dewatering system, the bottom is an oil-sewage outlet 802, the middle part of the side wall is provided with a second inlet 804 for flowing into the light oil-sewage separation device to discharge slurry and a third inlet 805 for flowing into the slurry at the bottom of the slurry pool of the desulfurization absorption tower, the side wall is further provided with a slurry outlet 806 which is higher than the second inlet 804 and the third inlet 805, and the slurry outlet 806 can be connected to a drainage pit of the desulfurization absorption tower region through a pipeline.
The utility model discloses an overall working principle as follows:
firstly, the oil-containing slurry 12 on the upper part of the slurry pool of the desulfurization absorption tower flows into a light oil separation device through an oil-containing slurry inlet 102, and is subjected to bubbling separation through a bubbling separation area, the slurry with high density is fully utilized to cooperate with bubbles to drive light oil dirt to float, so that the light oil dirt overflows from the top of the bubbling separation area and enters an oil storage pool 3, the high-concentration light oil dirt 13 in the oil storage pool 3 is directly discharged and treated, the oil-containing slurry at the bottom of the oil storage pool 3 is circulated back to the bubbling separation area again to be separated, and the heavy oil-containing slurry precipitated at the bottom of the bubbling separation area continuously enters a slurry buffer area 4 through a bottom coupling. Therefore, the light oil separation device can fully utilize the high density of the slurry to separate the light oil dirt and the slurry by means of air-blowing separation and recycling.
Then, the partial slurry is returned to the slurry 14 of the back-spray desulfurization absorbing tower shown in fig. 1, i.e., the slurry is returned to the back-spray desulfurization absorbing tower through the slurry, or the partial slurry is injected into the heavy oil separating device, i.e., the slurry 15 shown in fig. 1, depending on the operating conditions.
On the heavy oil dirt separation device 8, thick slurry 16 at the bottom of a slurry pool of the desulfurization absorption tower is simultaneously sent to the heavy oil dirt separation device 8 through a slurry pool sewage pump 11, in addition, filtrate and overflow 17 of a gypsum dehydration system are also injected into the heavy oil dirt separation device 8, separation is realized in the heavy oil dirt separation device 8 by utilizing slurry density reduction, finally separated high-purity heavy oil dirt 18 is discharged to be comprehensively utilized, and separated slurry 19 with less oil dirt overflows to a drainage pit of the desulfurization absorption tower area and returns to a desulfurization slurry system for recycling.
Example 2
Based on the design of example 1, as shown in fig. 1, the bubble separation zone is designed as a secondary separation zone, including a primary separation zone 1 and a secondary separation zone 2, and the primary separation zone 1 is communicated with the top of the secondary separation zone 2. Further, the partition plate 101 between the primary separation zone and the secondary separation zone 2 is at least 200mm higher than the partition plate 201 between the secondary separation zone 2 and the oil sump 3. After entering the primary separation zone 1, the slurry containing oil sludge can overflow from the top to the secondary separation zone 2 after being subjected to bubbling separation.
The bottom of the secondary and the last separation zones are provided with third slurry outlets 202, and the third slurry outlets 202 are connected to the first slurry circulating inlet 103 at the top of the bubbling separation zone through pipelines.
And a communicating hole 6 for slurry circulation is reserved between the bottom end of the partition plate between the bubbling separation zone and the slurry buffer zone 4 and the bottom plate of the light oil sewage separation device, so that the slurry flows conveniently, and the slurry liquid level of the bubbling separation zone is maintained. The height of the communication hole 6 is 150 mm.
The height of the bottom plate of the light oil sewage separation device from the position of the bubbling pipe network 5 close to the communicating hole 6 is 300 mm.
Example 3
On the basis of the design of the embodiment 1 or 2, as shown in fig. 1-2, a first stirring device 7 is arranged in the slurry buffer area 4 and is used for stirring and mixing the separated slurry at different times, so that the slurry is uniformly mixed and the density is consistent.
Example 4
Based on the design of embodiment 1, 2 or 3, as shown in fig. 1-2, further, the structure of the heavy oil pollution separation device 8 can be designed as a cylindrical mixing area at the upper part and a funnel-shaped sinking area at the lower part, and a second stirring device 801 is arranged in the mixing area and is used for stirring and mixing the heavy oil-containing slurry entering from different inlets, so that the heavy oil-containing slurry is uniformly mixed and has consistent density.
Example 5
On the basis of the design of any of the above embodiments, the pipeline can be further designed as follows:
a recirculation pump 9 is provided on a line connecting the first slurry discharge port 301 to the first slurry circulation inlet 103, and the slurry discharged from the oil sump 3 is pumped into the first slurry circulation inlet 103 by the recirculation pump 9; when a multi-separation structure is designed, the third slurry outlet 202 is connected to the front end of the recirculation pump 9, and the slurry discharged from the oil sump 3 is pumped into the first slurry circulation inlet 103 together with the slurry in the secondary separation zone 2 and the subsequent separation zones by the recirculation pump 9.
A slurry return pump 10 is provided in a line externally connected to the second slurry outlet 401, and the slurry return pump 10 is connected to a three-way line connected to the second slurry outlet 401.
For the third inlet 805 of the heavy oil pollution separation device 8, a slurry sewage pump 11 is arranged on an external inflow pipeline, and slurry at the bottom of a slurry pool of the desulfurization absorption tower is pumped into the heavy oil pollution separation device 8.
Example 6
According to the design of above-mentioned embodiment, in the aspect of the material, the utility model discloses suitable material has also been selected.
The wallboard, the partition board and the bubbling pipe network 5 of the light oil dirt separation device and the heavy oil dirt separation device 8 are made of stainless steel materials 316L.
The stirring blade of the stirring device adopts alloy 1.4529.
Proved after experiment and concrete implementation, above-mentioned material can effectively realize the utility model discloses a life can realize the separation of greasy dirt well, improves the desulfurization thick liquid quality.
By integrating the design of all the embodiments, the system automatically controls the sizes of bubbles, the switches of all the pumps and the like through an electric control system. Specific tests prove that under the condition of continuous operation, the oil stain removal rate of the system can reach more than 80 percent, the oil stain content in slurry is effectively reduced, the operation condition of a desulfurization system is improved, the normal operation of the desulfurization system is ensured, the gypsum quality is improved, and the system is suitable for being widely applied to the conventional desulfurization system.