EP0004253A2 - Corps de tube empilable muni d'une couche de matière d'étanchéité, procédé et appareil pour la fabrication d'un tel corps de tube - Google Patents
Corps de tube empilable muni d'une couche de matière d'étanchéité, procédé et appareil pour la fabrication d'un tel corps de tube Download PDFInfo
- Publication number
- EP0004253A2 EP0004253A2 EP79810022A EP79810022A EP0004253A2 EP 0004253 A2 EP0004253 A2 EP 0004253A2 EP 79810022 A EP79810022 A EP 79810022A EP 79810022 A EP79810022 A EP 79810022A EP 0004253 A2 EP0004253 A2 EP 0004253A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- tube
- tube body
- sealant
- material deformation
- jaws
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 239000000463 material Substances 0.000 title claims description 28
- 238000000034 method Methods 0.000 title claims description 11
- 238000004519 manufacturing process Methods 0.000 title description 7
- 238000007789 sealing Methods 0.000 claims abstract description 5
- 239000000565 sealant Substances 0.000 claims description 41
- 239000011324 bead Substances 0.000 claims description 22
- 238000007373 indentation Methods 0.000 claims description 4
- 238000003825 pressing Methods 0.000 claims description 2
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims 1
- 229910052782 aluminium Inorganic materials 0.000 claims 1
- 239000003566 sealing material Substances 0.000 abstract 5
- 230000006378 damage Effects 0.000 description 3
- 230000002787 reinforcement Effects 0.000 description 2
- 239000004925 Acrylic resin Substances 0.000 description 1
- 229920000178 Acrylic resin Polymers 0.000 description 1
- 239000000853 adhesive Substances 0.000 description 1
- 230000001070 adhesive effect Effects 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 238000000576 coating method Methods 0.000 description 1
- 230000006835 compression Effects 0.000 description 1
- 238000007906 compression Methods 0.000 description 1
- 238000005336 cracking Methods 0.000 description 1
- 239000006185 dispersion Substances 0.000 description 1
- 238000004806 packaging method and process Methods 0.000 description 1
- 239000003973 paint Substances 0.000 description 1
- 238000005096 rolling process Methods 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D35/00—Pliable tubular containers adapted to be permanently or temporarily deformed to expel contents, e.g. collapsible tubes for toothpaste or other plastic or semi-liquid material; Holders therefor
- B65D35/02—Body construction
Definitions
- the invention relates to a stackable, conical tube body, the open end of which is provided on the inside with a sealant for sealing closure on an annular sealant section.
- the invention also relates to a method for producing such tube bodies and to an apparatus for carrying out the method.
- Such stackable tube bodies allow a particularly space-saving and efficient packaging of the tube bodies for shipping to the bottler.
- the tubes After filling, the tubes are closed at the open end in the area of the sealant layer by folding them together.
- Such tubes were e.g. already known from DE-OS 25 22 511, in which the sealant consists of a wax-like mass. If the sealant layer consists of an adhesive, problems arise when stacking the tube bodies in that the stacked tubes must not touch the sealant under any circumstances.
- a conical tube body is already known from German Patent No. 2 009 692, the open end of which has an enlarged section with the same conicity as the tube jacket.
- the seal ring is applied inside this extended section.
- the diameter of the enlarged section is selected such that the sealant ring does not come into contact with the next inserted tube.
- the disadvantage of this configuration is that the tube walls touch directly when stacked one inside the other. As a result, the tubes adhere to one another to such an extent that, on the one hand, it is difficult to separate the tubes and, on the other hand, damage to the already printed tube surface is possible.
- Another disadvantage of the extended tube end is that when this area is folded together, edges that protrude outward relative to the tube body arise. These sharp-edged projections easily lead to injuries and also look unattractive.
- the expanded tube section also presents some difficulties in production, since longitudinal cracks can occur at the end of the tube if the necessary expansion is required.
- the object of the invention is, in particular, to avoid the disadvantages of the known and to create a stackable tube body which is simple to manufacture, with which a gentle stacking of the tube body is made possible and in which a reinforcement of the open tube end is also achieved.
- the tube body in addition to the sealant section for protecting the sealant when the tubes are stacked, is provided with at least one material deformation directed against the tube axis, and in that the inner diameter in the region of the material deformation is smaller than the inside diameter of the end region of the sealant layer adjacent to the material deformation.
- This inward-facing material deformation protects the immediately adjacent sealant section from contact with the inserted tube body.
- the material deformation also ensures that the tube walls do not touch directly. This protects the tube surface from damage, prevents the paint coating from sticking together and makes it easier to separate the tubes.
- the material deformation is arranged between the sealant section and the open tube end. With this arrangement, the sealant section is evidently always protected even with the stacked tubes.
- the invention can be implemented particularly simply and advantageously if the material deformation is designed as an annular bead.
- the advantage of this configuration is the reinforcement and stiffening of the entire edge area at the tube opening.
- the inside diameter can be dimensioned such that there is sufficient space between the tube shells without the bead having to have a radius that is too small.
- the depth of the bead is chosen so that the material deformation just rises above the layer thickness of the sealant layer. This requirement also applies if the bead does not have a semicircular cross-section.
- the bead can e.g. also have an approximately trapezoidal cross section. There is no risk of cracking in the bead according to the invention, since if the tube is deformed inwards, it is not stretched but compressed.
- the material deformation consists of two annular beads which are arranged on both sides of the sealant section.
- the second corrugation provides additional protection against radial loads on the tube casing that are effective from the outside.
- Such tube bodies are usually butted in a single operation. It would theoretically be conceivable to also apply the ring-shaped material deformations together with the butting. However, in order to make the tube body manufacturing process flexible and to be able to take into account special customer requirements, it is advantageous to separate the work processes and in certain cases even the material deformations only last, i.e. apply after applying the sealant layer. However, this poses particular problems in production, since the sealant layer makes it more difficult to clamp or center the tube body. For example, rolling of the depressions is not considered since it is not possible to insert a suitable holder into the tube.
- This object is achieved in that the tube is clamped from the outside in the region to be deformed, essentially over the entire circumference, and is deformed at least in a partial section of the circumference.
- the device has a holding mandrel for holding the tube body, the outer diameter of which is matched to the inner diameter of the tube at least in the front region and the outer diameter of which is smaller in the region of the portion of the tube to be deformed than the inner diameter of the tube that Holding mandrel for supporting the open tube end has a supporting device, and that at least three concentrically closable jaws are arranged around the holding mandrel for applying the deformation, the surface of which facing the tube wall is adapted in the closed state to the desired configuration of the material deformation.
- the special configuration of the holding mandrel clearly shows that the tube is held in a form-fitting manner in its front area, while it does not rest in the area of the deformation. This prevents the already applied sealant layer from coming into contact with the holding mandrel and sticking.
- the support device at the open end of the tube ensures easy expansion of the tube end.
- the concentrically lockable jaws allow material deformation of any configuration to be applied without damaging the relatively unstable and flexible tube body.
- the open tube end can be widened particularly optimally if the support device is a truncated cone that is adjustable in the axial direction on the holding mandrel. In this way, slightly compressed tube bodies are deformed back into an exactly conical starting position. The adjustability of the support device on the holding mandrel ensures a precise adjustment of the expansion. The widening at the end of the tube later makes it easier to separate the stacked tubes.
- the holding mandrel is provided with an ejection device for easier removal of the tube body from the device.
- This can be implemented in a particularly simple manner if the ejection device consists of a bore in the holding mandrel that can be fed with compressed air. Obviously, a short burst of compressed air is sufficient to eject the tube from the device.
- the advantage of this ejection device is that it does not require any moving parts.
- the jaws of the device can be moved particularly easily if they are surrounded by a common locking ring which can be moved in the axial direction and which has a conical inner wall for simultaneously pressing the jaws together. This ensures that all jaws are pressed against the tube jacket with the same force at the same time.
- the jaws on the outer wall are also particularly advantageously provided with a corresponding cone.
- the closing stroke of the jaws can be determined particularly easily by appropriately selecting the cone inclination.
- this type of jaw actuation ensures the use of mechanically simple actuation devices.
- a tube body 1 consists of a conical tube jacket 2, which ends at the front in a shoulder 4, to which the closure cap 3 is attached. When stacked one inside the other, the sealing caps 3 rest on the shoulder 4. The stacking division C is also determined by the height of the closure cap 3.
- a sealant layer 5 with a layer thickness E is applied to an annular sealant section with the width A.
- This sealant layer can consist, for example, of acrylic resin dispersion or of another suitable material.
- the tube end is provided with an inwardly directed bead 6, which has the width B and whose inner diameter D is smaller than the inner diameter of the end region 8 of the sealant layer adjacent to the material deformation. This dimensioning prevents the sealant layer from touching through the inserted tube at any conification angle.
- the bead 6 has a material deformation with the depth F, which rises by the amount F minus E over the layer thickness E of the sealant section.
- the inserted tube 1 1 is on the one hand supported on the shoulder 4 and the other hand to the bead. 6
- play should be provided between the bead 6 on the diameter D and the inserted tube.
- the space between the tube bodies 1 and 1 ' depends on the cone angle, on the stack pitch C and on the inside diameter D of the bead 6.
- the bead 6 reinforces the tube end in such a way that even when the tubes are stacked together, an unintentional compression in the sealant area A is no longer possible.
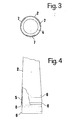
- FIG. 3 shows a modified embodiment in which the material deformation there are three partial indentations 7 lying on the same level.
- the material deformation could also be designed as a step-like depression.
- the sealant area A, the width B of the bead 6 and the stacking division C can also be changed as desired, depending on the circumstances and the tube configuration.
- the choice of the correct thickness of the sealant layer 5 is readily possible for the person skilled in the art and is not specified in more detail here.
- the tube body is held by a holding mandrel 9, which is adapted in its front area to the inside diameter of the tube.
- the outer diameter of the holding mandrel 9 in the region of the deformation or in the region of the sealant layer 5 is smaller than the inner diameter of the tube. In this way, the holding mandrel 9 does not come into contact with the sealant layer 5.
- the tube body 1 is pushed up to the shoulder 4 on the holding mandrel 9 by a feed device, not shown.
- the cap 3 is already screwed onto the tube body.
- the holding mandrel 9 is provided over its entire length with a bore 12 through which compressed air can be blown to expel the tube body.
- a support device 10 is provided, which is advantageously designed as a truncated cone. In order to be able to adapt the support device to the different tube lengths, it can be adjusted on the holding mandrel 9. When the tube body 1 is pushed onto the holding mandrel 9, the open tube end 16 is slightly widened on the conical support device 10.
- the support device is set in such a way that the open tube end 16 is reliably supported in any case even in the event of tolerance fluctuations in the tube length.
- the extension at the end of the tube has the advantage that the stacked tubes can later be separated more easily.
- the jaws 11 are mounted in a jaw guide 13, not shown in detail, and are radially displaceable. It has proven to be particularly advantageous if three concentrically displaceable jaws are used to apply the deformation. Of course, it is also possible to use a larger number of jaws.
- the jaws are actuated by a common locking ring 14.
- the locking ring comprises all jaws 11 and is connected to a push rod 15.
- the locking ring 14 has a conical inner wall 18 with which the jaws 11 are pushed together concentrically in the direction of arrow A. This is done by axially advancing the locking ring 14 with the aid of the push rod 15 in the direction of arrow B.
- the jaws 11 which are rigid in the axial direction and which are mounted in the jaw guide 13 are pressed together.
- the figure shows the device in the starting position above the center line and the device with pressed-on jaws 11 below the center line.
- the force required for actuating the push rod 15 is applied by an actuating device, not shown, which preferably consists of a hydraulic or pneumatic lifting cylinder.
- the cheek outer walls 19 are advantageously also conical. In this case, an axial force component is converted into a radial force component in a particularly simple manner by advancing the locking ring 14.
- the jaws can be operated in other ways. For example, it would be conceivable to move the individual jaws on the jaw guide using racks and bevel gears.
- the cheek surfaces 17 facing the tube jacket are provided with projections 20 which, on the conical tube jacket, produce the desired beads when the jaws are pressed together.
- the projections 20 can have any configuration. Even after the circular beads 6 have been pressed in, the tube jacket does not touch the holding mandrel 9 in this area.
- the method and the device allow a rational and flexible production of conical tube bodies of the type mentioned. With other tube dimensions, only the holding mandrel 9 or the jaws 11 need to be replaced. Depending on the type and nature of the sealant layer 5 can also. Jaws 11 with different jaw surfaces 17 can be used.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Shaping Of Tube Ends By Bending Or Straightening (AREA)
- Rigid Pipes And Flexible Pipes (AREA)
- Materials For Medical Uses (AREA)
- External Artificial Organs (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CH262178A CH626302A5 (fr) | 1978-03-10 | 1978-03-10 | |
| CH2621/78 | 1978-03-10 | ||
| CH1449/79 | 1979-02-14 | ||
| CH144979A CH634761A5 (en) | 1979-02-14 | 1979-02-14 | Method and apparatus for deforming a tubular body |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0004253A2 true EP0004253A2 (fr) | 1979-09-19 |
| EP0004253A3 EP0004253A3 (en) | 1979-10-03 |
| EP0004253B1 EP0004253B1 (fr) | 1980-09-03 |
Family
ID=25687686
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP79810022A Expired EP0004253B1 (fr) | 1978-03-10 | 1979-03-05 | Corps de tube empilable muni d'une couche de matière d'étanchéité, procédé et appareil pour la fabrication d'un tel corps de tube |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0004253B1 (fr) |
| AT (1) | AT364642B (fr) |
| DK (1) | DK146358C (fr) |
| NO (1) | NO790803L (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2511344A1 (fr) * | 1981-08-11 | 1983-02-18 | Ketels Tuben Vertriebs Gmbh | Tube souple conique destine a servir de recipient et procede d'obtention |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1877534A (en) * | 1931-12-19 | 1932-09-13 | Bond Mfg Corp | Collapsible tube |
| FR1223759A (fr) * | 1959-05-05 | 1960-06-20 | Tube souple et appareillage pour l'obtention de ce tube | |
| DE1938943C3 (de) * | 1969-07-31 | 1974-05-30 | Siemens Ag, 1000 Berlin Und 8000 Muenchen | Abdeckkappe für ein Probengefäß |
| DE2008885A1 (de) * | 1970-02-26 | 1971-09-09 | CF Spiess & Sohn, 6719 Kleinkarl bach | Tube und Vorrichtung zur Herstellung |
| DE2447420A1 (de) * | 1974-10-04 | 1976-04-15 | Viw Verbundene Industriewerke | Zur bildung einer tubenstange geeigneter tubenrohling, verfahren zu seiner herstellung und aus ihm gebildete tubenstange |
-
1979
- 1979-03-05 EP EP79810022A patent/EP0004253B1/fr not_active Expired
- 1979-03-08 AT AT0173879A patent/AT364642B/de not_active IP Right Cessation
- 1979-03-09 NO NO790803A patent/NO790803L/no unknown
- 1979-03-09 DK DK98979A patent/DK146358C/da not_active Application Discontinuation
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2511344A1 (fr) * | 1981-08-11 | 1983-02-18 | Ketels Tuben Vertriebs Gmbh | Tube souple conique destine a servir de recipient et procede d'obtention |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0004253B1 (fr) | 1980-09-03 |
| DK98979A (da) | 1979-09-11 |
| AT364642B (de) | 1981-11-10 |
| ATA173879A (de) | 1981-03-15 |
| DK146358B (da) | 1983-09-19 |
| NO790803L (no) | 1979-09-11 |
| DK146358C (da) | 1984-03-12 |
| EP0004253A3 (en) | 1979-10-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE2113235C3 (de) | Verfahren und Vorrichtung zum Formen eines integralen Hohlniets an einem Blechteil | |
| DE4446506A1 (de) | Vorrichtung zum Aufweiten von Hohlkörpern | |
| DE19730054C1 (de) | Expansionswerkzeug zum Verformen rohrförmiger Werkstückenden | |
| DE1966897A1 (de) | Kegelspreizdorn zum aufweiten von tuben | |
| DE2240148B2 (de) | Dorn für eine hydrostatische Strangpresse zum Herstellen von Rohren mit profiliertem Innenquerschnitt | |
| EP0004253B1 (fr) | Corps de tube empilable muni d'une couche de matière d'étanchéité, procédé et appareil pour la fabrication d'un tel corps de tube | |
| DE19820124C2 (de) | Verfahren zur Herstellung eines Rohres zur Verwendung in einem Lenkgestänge | |
| DE1924716C3 (de) | Verfahren und Vorrichtung zum Beseitigen von Beulen und asymmetrischen Spannungen an der Seitenwand bzw. dem Mantel oder Mantelteil von zylindrischen Behältern aus Metallblech mit festgelegter SoU-Abmessung | |
| DE4339993C1 (de) | Vorrichtung zum Aufweiten von Hohlkörpern | |
| DE2738863C3 (de) | Vorrichtung zum konischen Aufweiten von Tuben | |
| DE102019001741B4 (de) | Packtulpe zum kopfseitigen Ergreifen von Flaschen | |
| DE2539354A1 (de) | Verfahren und vorrichtung zum herstellen von leichtbehaeltern | |
| DE1757712A1 (de) | Verfahren und Vorrichtung zum Verschliessen eines Behaelters mittels einer Kappe | |
| DE2418104A1 (de) | Hydraulische presse | |
| DE2901169B2 (de) | Vorrichtung zum Falten und Anpressen einer auf dem Hals einer Flasche o.dgl. sitzenden Flaschenkapsel | |
| CH634761A5 (en) | Method and apparatus for deforming a tubular body | |
| EP0791132B1 (fr) | Procede et dispositif de fabrication d'un bloc en nid d'abeilles, en particulier un bloc-support de catalyseur avec enveloppe | |
| DE2743998C2 (de) | Konischer Tubenrohling und Vorrichtung zum konischen Aufweiten eines Tubenrohlings | |
| EP0512426B1 (fr) | Procédé et dispositif pour la réalisation de filetages sur des tubes polygonales | |
| DE2131504C3 (de) | Vorrichtung zum Konischweiten von Metalltuben | |
| DE2202878C3 (de) | Verfahren zum Verbinden von Draht oder Stangen aus Verbundmaterial mit Aluminiumkern und Kupfermantel | |
| DE2052080C3 (de) | Vorrichtung zum Herstellen von konischen Tuben oder Hülsen | |
| DE2820324C3 (de) | Vorrichtung zum konischen Aufweiten von Metalltuben | |
| WO2009080001A1 (fr) | Procédé et dispositif pour fabriquer un filetage, pièce et appareil | |
| DE4207841C2 (de) | Stopfen für einen Behälter und Verfahren zur Herstellung des Stopfens |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Designated state(s): DE FR GB IT NL SE |
|
| AK | Designated contracting states |
Designated state(s): DE FR GB IT NL SE |
|
| 17P | Request for examination filed | ||
| ITF | It: translation for a ep patent filed | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Designated state(s): DE FR GB IT NL SE |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19840229 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 19840331 Year of fee payment: 6 Ref country code: NL Payment date: 19840331 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19840413 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19850306 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19851001 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19851129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19851203 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee | ||
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19881117 |
|
| EUG | Se: european patent has lapsed |
Ref document number: 79810022.8 Effective date: 19860128 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |