EP0012853A1 - Vorrichtung in Form eines Korbes zum Transportieren von Schüttgut durch Warmbehandlungsöfen - Google Patents
Vorrichtung in Form eines Korbes zum Transportieren von Schüttgut durch Warmbehandlungsöfen Download PDFInfo
- Publication number
- EP0012853A1 EP0012853A1 EP79104648A EP79104648A EP0012853A1 EP 0012853 A1 EP0012853 A1 EP 0012853A1 EP 79104648 A EP79104648 A EP 79104648A EP 79104648 A EP79104648 A EP 79104648A EP 0012853 A1 EP0012853 A1 EP 0012853A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- basket
- insert
- bulk material
- heat
- treatment furnaces
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 239000013590 bulk material Substances 0.000 title claims abstract description 20
- 238000010438 heat treatment Methods 0.000 title claims abstract description 5
- 239000000463 material Substances 0.000 description 4
- 239000002184 metal Substances 0.000 description 4
- 230000008646 thermal stress Effects 0.000 description 3
- 229910000831 Steel Inorganic materials 0.000 description 2
- 238000005245 sintering Methods 0.000 description 2
- 239000007787 solid Substances 0.000 description 2
- 239000010959 steel Substances 0.000 description 2
- 238000005256 carbonitriding Methods 0.000 description 1
- 238000005255 carburizing Methods 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- JEIPFZHSYJVQDO-UHFFFAOYSA-N iron(III) oxide Inorganic materials O=[Fe]O[Fe]=O JEIPFZHSYJVQDO-UHFFFAOYSA-N 0.000 description 1
- 238000005121 nitriding Methods 0.000 description 1
- 230000035699 permeability Effects 0.000 description 1
- 238000010791 quenching Methods 0.000 description 1
- 230000000171 quenching effect Effects 0.000 description 1
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/0006—Details, accessories not peculiar to any of the following furnaces
- C21D9/0025—Supports; Baskets; Containers; Covers
Definitions
- the invention relates to a device in the form of a basket for transporting bulk material in rigid piles through heat treatment furnaces, the heated bulk material being dumped out of the basket.
- the material to be treated is grilled with the help of rust if it is a single piece of large size, or in trays, boxes or baskets if it is a matter of small dimensions Oven transported. If the parts are then to be quenched, the loaded grids, trays, boxes and baskets can be tipped over the quenching bath. At the high temperatures of up to 1000 ° C, to which the material to be treated is heated, the individual parts of bulk material tend to stick to one another and to the container. To ensure complete emptying, the containers are turned around Tilted up to 180 ° and shaken with a vibrator if necessary.
- the present invention is based on the object of improving a basket of the type mentioned in such a way that wedging of the bulk goods with one another and with the transport basket is reliably avoided and complete emptying when tipping is achieved.
- the insert is preferably a cylinder or a cone which tapers upwards.
- the insert is divided in the longitudinal direction into two halves, which are loosely connected to one another.
- the insert is designed as a cone, the bulk material can deflect upwards. If the insert is furthermore divided into two halves, which are loosely connected to one another or inserted loosely into one another, the flexibility of the insert against thermal stresses of the bulk material is additionally improved.
- the insert is set loosely has no disadvantages when filling the bulk material.
- the insert essentially always has the desired basic shape, i.e. Cylindrical or conical shape.
- the holder for the insert is preferably a rod or a tube, projects across the basket wall and insert in the upper region of the basket and is fastened to the basket wall. This type of holder has the additional advantage that the bulk material falling out of the basket when tipped is loosened.
- a base 1 which is designed as a solid frame in welded or cast construction.
- a flat sheet 3 provided with openings, which forms the bottom of the basket.
- the basket wall 3 is also made of perforated sheet metal, so that furnace heat and furnace atmosphere have as unimpeded access to the bulk material 8 to be treated as possible.
- an insert 7 also made of perforated sheet metal is loosely set.
- a rod 4 is used, which is inserted across the basket wall 3 and insert 7 in the upper region of the basket and on the basket wall 3, for example by a Weld 5 is attached.
- 4 cams 6 are attached to the rod.
- the insert 7 like the basket wall 3 and basket base 2, consists of either a high-temperature-resistant steel or a simple bulk steel. Perforated sheet metal, expanded metal or wire mesh is preferably used as the material to ensure good gas and heat permeability.
- the bulk material 8 to be heat-treated is located between the basket outer wall 3 and the basket insert 7. The basket insert 7 is able, due to its loose parts, to yield and compensate for thermal stresses in the bulk material 8.
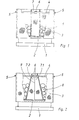
- FIG. 2 shows an embodiment with a conical insert.
- the basket and insert are made of gas and heat-permeable material; For better clarity, however, the parts are shown as solid sheets.
- the conical shape of the insert 7 additionally facilitates the reduction of thermal stresses in the bulk material 8.
- the insert 7 is divided into two parts 7.1 and 7.2 along a dividing line 9 which extends in the longitudinal direction, it being noted here that such a division can also be used with a cylindrical insert as in FIG. As a result of this division, the two parts of the insert 7 can additionally shift relative to one another, whereby an even better reduction of thermal tensions in the bulk material 8 is possible.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Furnace Charging Or Discharging (AREA)
- Heat Treatments In General, Especially Conveying And Cooling (AREA)
Abstract
Description
- Die Erfindung betrifft eine Vorrichtung in Form eines Korbes zum Transportieren von Schüttgut in starren Haufwerken durch Warmbehandlungsöfen, wobei das erhitzte Schüttgut aus dem Korb ausgekippt wird.
- In Warmbehandlungsöfen zum Gasaufkohlen, Nitrieren, Karbonitrieren oder Blankhärten wird das zu behandelnde Gut mit Hilfe von Rosten, wenn es sich um ein Einzelstück großer Abmessung handelt, oder in Schalen, Kästen bzw. Körben, wenn es sich um Schüttgut kleiner Abmessungen handelt, durch den Ofen transportiert. Sollen die Teile anschließend'äbge- schreckt werden, so kann man die beladenen Roste, Schalen, Kästen und Körbe über dem Abschreckbad kippen. Bei den hohen Temperaturen von bis 1000°C, auf die das zu behandelnde Gut aufgeheizt wird, neigen bei Schüttgut die einzelnen Teile zum Verkleben untereinander und mit dem Behälter. Um eine völlige Entleerung zu gewährleisten, werden die Behälter um bis zu 180° gekippt und ggf. mit einer Rütteleinrichtung gerüttelt.
- Trotz dieser Maßnahmen ist immer wieder zu beobachten, daß nicht alle Teile aus den Transportkorb herausfallen. Dies ist darauf zurückzuftren, daß die Teile bei den hohen Temberaturen mitelrander oberflächlich versintern und daß sichder dehnung untereinander und mit der Transportkorb verkeilen. Eine zusätzliche Rütteleinrich- tang verteuert darüberhisaus die Anlage.

- Der vorliegenden Erfindung-liegt die Aufgabe zugrunde, einen Korb der eingangs genannten Art dahingehend zu verbessern, daß das Verkeilen des Schüttgutes untereinander und mit dem Transportkorb sicher vermieden und damit ein vollständiges Entleeren beim Kippen erreicht wird.
- Diese Aufgabe wird dadurch gelöst, daß in den Korb ein korbartiger Einsatz lose, aber gegen Herausfallen gesichert, eingestellt ist.
- Vorzugsweise ist der Einsatz ein Zylinder oder ein Kegel, der sich nach oben verjüngt.
- Gemäß einer vorteilhaften Weiterbildung ist der Einsatz in Längsrichtung in zwei Hälften geteilt, die lose miteinander verbunden sind.
- Damit ergeben sich die Vorteile, daß der lose eingestellte Einsatz der Wärmedehnung des Schüttgutes ausweichen kann, so daß keine Verkeilung mehr stattfindet. Ist der Einsatz als Kegel ausgebildet, so kann das Schüttgut nach oben ausweichen. Ist der Einsatz darüberhinaus in zwei Hälften geteilt, die lose miteinander verbunden bzw. lose ineinander gesteckt sind, so ist die Nachgiebigkeit des Einsatzes gegenüber Wärmespannungen des Schüttgutes zusätzlich verbessert.
- Die Erfahrung hat gezeigt, daß die Tatsache, daß der Einsatz lose eingestellt ist, keine Nachteile beim Einfüllen des Schüttgutes hat. Insbesondere hat sich gezeigt, daß auch dann, wenn der Einsatz aus zwei Teilen besteht, der Einsatz im wesentlichen immer die gewünschte Grundform, d.h. Zylinder- oder Kegelform, annimmt.
- Vorzugsweise ist die Halterung für den Einsatz eine Stange bzw. ein Rohr, ragt im oberen Bereich des Korbes quer durch Korbwand und Einsatz und ist an der Korbwand befestigt. Diese Art der Halterung hat den zusätzlichen Vorteil, daß das beim Kippen aus dem Korb herausfallende Schüttgut aufgelockert wird.
- Anhand der Zeichnung soll die Erfindung in Form von Ausführungsbeispielen näher erläutert werden.
-
- Fig. 1 zeigt in teilweise geschnittener Darstellung einen Kippkorb mit zylindrischem Einsatz,
- Fig. 2 zeigt ebenfalls in teilweise geschnittener Darstellung einen Kippkorb mit kegelförmigem Einsatz.
- Man erkennt einen Sockel 1, der als massiver Rahmen in Schweiß- bzw. Gußkonstruktion ausgebildet ist. Auf der Oberseite des Sockels 1 befindet sich ein ebenes, mit Öffnungen versehenes Blech 3, welches den Boden des Korbes bildet. Die Korbwand 3 ist ebenfalls aus gelochtem Blech hergestellt, damit Ofenwärme und Ofenatmosphäre einen möglichst ungehinderten Zugang zu dem zu behandelnden Schüttgut 8 haben. Im Inneren des Korbes ist ein ebenfalls aus gelochtem Blech hergestellter Einsatz 7 lose eingestellt. Zur Sicherung gegen Herausfallen des Einsatzes 7 beim Kippen des Korbes dient eine Stange 4, die im oberen Bereich des Korbes quer durch Korbwand 3 und Einsatz 7 gesteckt und an der Korbwand 3 beispielsweise durch eine Schweißnaht 5 befestigt ist. Um im Bedarfsfälle verhindern zu können, daß der Einsatz 7 auf der Haltestange 4 bis zur Korbwand 3 rutschen kann, sind an der Stange 4 Nocken 6 angebracht.
- Der Einsatz 7 besteht ebenso wie Korbwand 3 und Korbboden 2 aus entweder einem hochtemperaturfesten Stahl oder einem einfachen Massenstahl. Als Material findet vorzugsweise Lochblech, Streckmetall oder Drahtgeflecht Verwendung, um eine gute Gas- und Wärmedurchlässigkeit zu gewährleisten. Das wärmezubehandelnde Schüttgut 8 befindet sich zwischen der Korbaußenwand 3 und dem Korbeinsatz 7. Der Korbeinsatz 7 ist aufgrund seiner Lose in der Lage, Wärmespannungen des Schüttgutes 8 nachzugeben und auszugleichen.
- Figur 2 zeigt eine Ausführungsform mit kegelförmigem Einsatz. Zwar werden auch bei dieser Ausführungsform Korb und Einsatz aus gas- und wärmedurchlässigem Material hergestellt; der besseren Übersichtlichkeit wegen sind jedoch die Teile als Massivbleche dargestellt. Man erkennt sofort, daß die Kegelform des Einsatzes 7 den Abbau thermischer Spannungen im Schüttgut 8 zusätzlich erleichtert. Darüberhinaus ist bei diesem Ausführungsbeispiel der Einsatz 7 entlang einer in Längsrichtung sich erstreckenden Trennlinie 9 in zwei Teile 7.1 und 7.2 geteilt, wobei hier angemerkt werden soll, daß eine derartige Teilung auch bei einem zylindrischen Einsatz wie in Figur 1 anwendbar ist. Durch diese Aufteilung können sich die beiden Teile des Einsatzes 7 zusätzlich gegeneinander verschieben, wodurch ein noch besserer Abbau thermischer Spannungen im Schüttgut 8 möglich ist.
- Beim Kippen des Korbes fällt das durch Versintern der Oberflächen zu einem gewissen Grad miteinander verbackene Schüttgut 8 gegen die quer liegende Haltestange 4, wodurch diese Versinterungen aufgebrochen und das Schüttgut aufgelockert wird.
Claims (6)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT79104648T ATE559T1 (de) | 1978-12-23 | 1979-11-22 | Vorrichtung in form eines korbes zum transportieren von schuettgut durch warmbehandlungsoefen. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19782856041 DE2856041A1 (de) | 1978-12-23 | 1978-12-23 | Vorrichtung in form eines korbes zum transportieren von schuettgut durch warmbehandlungsoefen |
| DE2856041 | 1978-12-23 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0012853A1 true EP0012853A1 (de) | 1980-07-09 |
| EP0012853B1 EP0012853B1 (de) | 1982-01-13 |
Family
ID=6058316
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP79104648A Expired EP0012853B1 (de) | 1978-12-23 | 1979-11-22 | Vorrichtung in Form eines Korbes zum Transportieren von Schüttgut durch Warmbehandlungsöfen |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0012853B1 (de) |
| AT (1) | ATE559T1 (de) |
| DE (1) | DE2856041A1 (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE10315354A1 (de) * | 2003-04-03 | 2004-10-28 | Otto Junker Gmbh | Glühgestell |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1854179A (en) * | 1930-05-26 | 1932-04-19 | Chicago Steel Foundry Company | Metallurgical device |
| GB377371A (en) * | 1931-06-06 | 1932-07-28 | Charles Bailey | Improvements in means for supporting earthenware during firing |
| DE560654C (de) * | 1931-07-29 | 1932-10-05 | Alfred Scheller | Schmelzkorb zum Brennen keramischer Gegenstaende |
| US2962273A (en) * | 1958-04-22 | 1960-11-29 | Cambridge Wire Cloth | Material handling basket |
-
1978
- 1978-12-23 DE DE19782856041 patent/DE2856041A1/de not_active Ceased
-
1979
- 1979-11-22 AT AT79104648T patent/ATE559T1/de not_active IP Right Cessation
- 1979-11-22 EP EP79104648A patent/EP0012853B1/de not_active Expired
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US1854179A (en) * | 1930-05-26 | 1932-04-19 | Chicago Steel Foundry Company | Metallurgical device |
| GB377371A (en) * | 1931-06-06 | 1932-07-28 | Charles Bailey | Improvements in means for supporting earthenware during firing |
| DE560654C (de) * | 1931-07-29 | 1932-10-05 | Alfred Scheller | Schmelzkorb zum Brennen keramischer Gegenstaende |
| US2962273A (en) * | 1958-04-22 | 1960-11-29 | Cambridge Wire Cloth | Material handling basket |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE10315354A1 (de) * | 2003-04-03 | 2004-10-28 | Otto Junker Gmbh | Glühgestell |
| US7790100B2 (en) | 2003-04-03 | 2010-09-07 | Otto Junker Gmbh | Annealing rack |
Also Published As
| Publication number | Publication date |
|---|---|
| ATE559T1 (de) | 1982-01-15 |
| DE2856041A1 (de) | 1980-07-10 |
| EP0012853B1 (de) | 1982-01-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE2804338C2 (de) | Durchlauf-Ofen zur Wärmebehandlung von Kleinteilen | |
| DE2456771C2 (de) | Ofen zum kontinuierlichen Einschmelzen von Metallstücken oder -spänen | |
| EP0012853B1 (de) | Vorrichtung in Form eines Korbes zum Transportieren von Schüttgut durch Warmbehandlungsöfen | |
| DE2461402B2 (de) | Vorrichtung zum Beschicken eines Schachtofens mit wenigstens zwei verschiedene TeilchengröOen aufweisenden Feststoffpartikeln | |
| DE2057717A1 (de) | Vorrichtung zur Behandlung fester Partikel | |
| EP0481167B1 (de) | Vertikalschachtofen zum Wärmebehandeln von metallischen Werkstücken | |
| DE609105C (de) | Vorrichtung zum Einfuehren von Gattierungs- oder sonstigen Zusaetzen in im Giessereischachtofen erschmolzenes Eisen | |
| DE1758058A1 (de) | Vorrichtung zur Waermebehandlung | |
| DE3412771A1 (de) | Korb zum transportieren von schuettgut durch warmbehandlungsoefen | |
| DE2425232B1 (de) | Verfahren zum Grafitieren von aus Hartbrandkohle bestehenden Formkoerpern | |
| DE340232C (de) | Einrichtung zur mechanischen Reinigung des Rostes und Verteilung der Beschickung beiGeserzeugern oder Schachtoefen | |
| DE2352080B2 (de) | Gleitschutz- und/oder reifenschutzkette | |
| DE2749940A1 (de) | Behaelter zum behandeln von stueckigen, bzw. koernigen materialien | |
| DE19933428C1 (de) | Plattenbandofen | |
| DE2217524A1 (de) | Foerderplatte aus keramischem werkstoff fuer plattendurchschuboefen | |
| DE8802597U1 (de) | Trägergestell für eine Mehrzahl kleinerer Teile | |
| DE253350C (de) | ||
| DE2457902C3 (de) | Drehherdofen | |
| DE242512C (de) | ||
| DE3020149C2 (de) | Hubbalkenofen für die Wärmebehandlung von zunderbildenden metallischen Gegenständen | |
| DE2541993C3 (de) | Schachtofen zum Brennen und Sintern von stückigem Gut | |
| DE3920951C2 (de) | ||
| DE2835810A1 (de) | Vorrichtung zum auskippen von in einem chargenbehaelter enthaltenem waermebehandlungsgut | |
| DE1258439B (de) | Ofen mit einer einen Drehherd umschliessenden Ofenhaube zum Erwaermen von Knueppelstuecken und aehnlichen Werkstuecken auf Schmiedehitze | |
| DE3605726C1 (de) | Durchlaufofen zum Waermen und anschliessenden Abkuehlen von Werkstuecken |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): AT CH FR GB |
|
| 17P | Request for examination filed |
Effective date: 19801002 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Designated state(s): AT CH FR GB |
|
| REF | Corresponds to: |
Ref document number: 559 Country of ref document: AT Date of ref document: 19820115 Kind code of ref document: T |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19830729 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 19830815 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 19861024 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Effective date: 19871122 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Effective date: 19871130 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19881118 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |