EP0035568B1 - Ziegelsteinformmaschine - Google Patents
Ziegelsteinformmaschine Download PDFInfo
- Publication number
- EP0035568B1 EP0035568B1 EP80900184A EP80900184A EP0035568B1 EP 0035568 B1 EP0035568 B1 EP 0035568B1 EP 80900184 A EP80900184 A EP 80900184A EP 80900184 A EP80900184 A EP 80900184A EP 0035568 B1 EP0035568 B1 EP 0035568B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- mould
- support
- plungers
- assembly
- brick forming
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B17/00—Details of, or accessories for, apparatus for shaping the material; Auxiliary measures taken in connection with such shaping
- B28B17/009—Changing the forming elements, e.g. exchanging moulds, dies
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B3/00—Producing shaped articles from the material by using presses; Presses specially adapted therefor
- B28B3/02—Producing shaped articles from the material by using presses; Presses specially adapted therefor wherein a ram exerts pressure on the material in a moulding space; Ram heads of special form
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/02—Dies; Inserts therefor; Mounting thereof; Moulds
- B30B15/026—Mounting of dies, platens or press rams
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/02—Dies; Inserts therefor; Mounting thereof; Moulds
- B30B15/028—Loading or unloading of dies, platens or press rams
Definitions
- This invention relates to a forming apparatus for bricks or the like.
- Known brick forming apparatus disclosed for example in DE - A - 2245853 includes a mould for receiving brick forming material, a vertically reciprocable mould support arranged to support the mould, and upper and lower plungers adapted to compact therebetween the material within the mould.
- the upper plunger may be driven by a hydraulic cylinder secured to an upper portion of the machine to press the brick material in the mould against a stationary lower plunger.
- the mould support is typically driven by hydraulic cylinders mounted on right and left columns of the machine such that the mould is firmly supported while the brick is being pressed.
- the present invention is characterised in that the mould support is provided with a sideways facing opening permitting lateral insertion or removal of an assembly of mould and plungers into or from said support.
- the time required for changing moulds is reduced as compared with conventional brick forming machines and thus a higher efficiency in brick production is achieved.
- a combination of mould and upper and lower plungers with particular dimensions can as an assembly be rapidly put into and withdrawn from the mould support thus enabling ready replacement of mould and plungers when the brick size is to be changed.
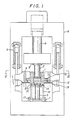
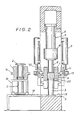
- brick forming apparatus includes a metallic mould 1 which receives brick forming material.
- the mould 1 is supported by a metallic mould support 4 which is reciprocable in a vertical direction and is driven by hydraulic cylinders 5.
- a movable upper plunger 2 is driven via a pressing block 8 by hydraulic cylinders 9 mounted on an upper frame 6 of the machine via a pressing block 8 and is effective in operation to compact downwardly the material in the mould 1 against a stationary lower plunger 3.
- the mould support and mould may then be pulled downwardly to the position shown in broken lines in Figures 1 and 2 to allow removal of the formed brick from the apparatus.
- the mould support 4 includes two pairs of wedges 11 located in front of and behind the mould 1, the wedges being driven by hydraulic cylinders 10 to advance and retract. In the advanced position the wedges engage inclined surfaces formed on flanges 30 provided on the front and rear sides of the mould 1, and thus firmly secure the mould in place.
- the mould 1 and the plungers 2, 3 form a detachable assembly which may conveniently as a whole be placed into and removed from the brick forming apparatus as described below, and this minimises the time delay involved in changing the mould 1, and plungers 2 and 3.
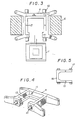
- the mould support 4 is in the form of a square frame one side of which is open and thus is generally U-shaped as viewed from above.
- the mould 1 and upper and lower plungers 2, 3 are assembled together prior to insertion into the apparatus and are placed into the mould support 4, via its front opening.
- the flanges 30 of the mould 1 are above the support 4, and thus the mould 1, together with the plungers 2, 3, may be moved into the apparatus by means of a transfer truck 16 and into the mould support via the front opening thereof.
- the mould support 4 is raised, the bottom flange of the mould support 4 will contact the flanges 30 of the mould 1 and thus the mould is seated snugly.
- the transfer truck 16 has upwardly protruding pins 15, which fit into holes 14 on the underside of the mould 1 to position it correctly when on the truck.
- the underside of the transfer truck 16 is provided with rollers 17, which roll back and forth on transfer rails 19 and positioning rails 7.
- the transfer truck is also generally U-shaped as viewed from above and thus includes an open end end through which the lower plunger 3 passes when the assembly of mould and plungers is removed from or placed on the truck.
- the assembly of mould 1 and the upper and lower plungers 2, 3 is replaced by moving the transfer truck 16 through the opening of the U-shaped mould support 4 such that the assembly is centred relative to the mould support 4; the transfer truck 16 is stopped at the correct position by a stopper 18 at the end of the positioning rails 7.
- the mould support 4 is then raised by the hydraulic cylinders 5. As the mould support 4 moves upwardly engagement of the pins 12 with the holes 13 guides the flanges 30 of the mould 1 to position it correctly on the mould support 4. As the mould support 4 ascends further the mould 1 and the upper and lower plungers 2, 3 are lifted from the transfer truck 16, and the truck 16 may be moved to the left as shown in Fig. 2 out of the apparatus.
- the mould 1 is secured to the support 4 by the advance of the hydraulic cylinders 10 and wedges 11, and the mould support 4 is then raised further such that the upper plunger 2 engages and may be for example bolted to the pressing block 8. Then the mould 4 is lowered until the bottom of the lower plunger hits the bottom face of the frame 6 to which the lower plunger may be secured by means of bolts or the like. This concludes the installation of a new assembly of mould and plungers.
- the removal of the mould 1 from the apparatus follows the above steps in reverse order.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Ceramic Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Press-Shaping Or Shaping Using Conveyers (AREA)
Claims (5)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP49249/79 | 1979-04-20 | ||
| JP4924979A JPS55140512A (en) | 1979-04-20 | 1979-04-20 | Molding machine used for brick* etc* |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0035568A4 EP0035568A4 (de) | 1981-09-07 |
| EP0035568A1 EP0035568A1 (de) | 1981-09-16 |
| EP0035568B1 true EP0035568B1 (de) | 1984-02-15 |
Family
ID=12825568
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP80900184A Expired EP0035568B1 (de) | 1979-04-20 | 1980-11-04 | Ziegelsteinformmaschine |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0035568B1 (de) |
| JP (1) | JPS55140512A (de) |
| DE (1) | DE2966698D1 (de) |
| WO (1) | WO1980002250A1 (de) |
Families Citing this family (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5002711A (en) * | 1984-07-11 | 1991-03-26 | Chiyoda Technical & Industrial Company Ltd. | Method and apparatus for setting pattern frame and press die in instant-release type molding machine for concrete product |
| IT1201805B (it) * | 1986-09-02 | 1989-02-02 | Daniele & C Officine Meccanich | Dispositivo movimentazione cesta in zona carico rottami |
| IT1201806B (it) * | 1986-09-02 | 1989-02-02 | Danieli Off Mecc | Perfezionamenti alle presse per pressare rottami nelle ceste, presse cosi' perfezionate e procedimento di movimentazione ceste sotto pressa |
| US4880373A (en) * | 1988-04-28 | 1989-11-14 | The Upjohn Company | Tablet press |
| JPH0755488B2 (ja) * | 1989-12-06 | 1995-06-14 | 株式会社三石深井鐵工所 | 金型交換方法及び装置 |
| FR2700137B1 (fr) * | 1993-01-05 | 1995-02-10 | Allibert Ind | Dispositif pour la fixation de moules d'injection sur les plateaux d'une presse. |
| IT1275537B (it) * | 1995-07-14 | 1997-08-07 | Siti Spa | Dispositivo atto ad essere utilizzato con un apparato di pressatura |
| FR2857899B1 (fr) | 2003-07-22 | 2005-11-18 | Cogema | Presse a compacter |
| JP5256065B2 (ja) * | 2009-01-30 | 2013-08-07 | 株式会社タイガーマシン製作所 | 型枠換え装置 |
| CN103302726A (zh) * | 2013-06-14 | 2013-09-18 | 王庆起 | 一种生产打孔水泥预制品的制砖机 |
| CN106900890B (zh) * | 2017-02-13 | 2023-09-26 | 湖北省农业科学院果树茶叶研究所 | 一种全自动砖茶成型设备 |
Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2245853A1 (de) * | 1972-09-19 | 1974-04-04 | Mitsuishi Fukai Iron Works | Steuervorrichtung fuer ziegelsteinschlagpressen |
Family Cites Families (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1312900A (fr) * | 1962-01-29 | 1962-12-21 | Danly Machine Specialties | Dispositif de serrage pour une presse à changement rapide de matrices |
| US3335657A (en) * | 1966-05-26 | 1967-08-15 | Minster Machine Co | Press with sliding bolster and die clamp |
| DE1945864C3 (de) * | 1968-09-13 | 1973-04-26 | Hitachi Ltd | Vertikalschere |
| US3559522A (en) * | 1969-01-28 | 1971-02-02 | Manco Mfg Co | Interchangeable die units for hydraulic presses |
| JPS4924506B1 (de) * | 1969-05-14 | 1974-06-24 | ||
| GB1243864A (en) * | 1969-08-22 | 1971-08-25 | Frederik Isaakovich Kaganovsky | Movable tool loading table for a hydraulic press |
| DE1955193C3 (de) * | 1969-11-03 | 1975-06-19 | Trumpf & Co, 7257 Ditzingen | Halter zum Einsetzen und Entnehmen eines Werkzeuges in eine bzw. aus einer Maschine |
| JPS4844307A (de) * | 1971-08-02 | 1973-06-26 | ||
| JPS5242132Y2 (de) * | 1971-07-19 | 1977-09-24 | ||
| JPS5234787B2 (de) * | 1971-08-25 | 1977-09-05 | ||
| DE2544711C3 (de) * | 1975-10-07 | 1983-06-01 | Georg 7203 Fridingen Fellner | Schnellspannwerkzeug für Schmiedepressen |
| DE2613213A1 (de) * | 1976-03-27 | 1977-10-06 | Amsted Siemag Kette Gmbh | Presse oder stanzmaschine |
| JPS5336779A (en) * | 1976-09-17 | 1978-04-05 | Yoshitsuka Seiki Kk | Powder molding machine |
-
1979
- 1979-04-20 JP JP4924979A patent/JPS55140512A/ja active Granted
- 1979-12-24 WO PCT/JP1979/000324 patent/WO1980002250A1/ja not_active Ceased
- 1979-12-24 DE DE8080900184T patent/DE2966698D1/de not_active Expired
-
1980
- 1980-11-04 EP EP80900184A patent/EP0035568B1/de not_active Expired
Patent Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2245853A1 (de) * | 1972-09-19 | 1974-04-04 | Mitsuishi Fukai Iron Works | Steuervorrichtung fuer ziegelsteinschlagpressen |
Also Published As
| Publication number | Publication date |
|---|---|
| JPS5745642B2 (de) | 1982-09-29 |
| WO1980002250A1 (fr) | 1980-10-30 |
| EP0035568A4 (de) | 1981-09-07 |
| JPS55140512A (en) | 1980-11-04 |
| EP0035568A1 (de) | 1981-09-16 |
| DE2966698D1 (en) | 1984-03-22 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4462783A (en) | Mechanism for exchanging molding dies in an injection molding machine | |
| US4631015A (en) | Molding apparatus with replaceable plunger and die set | |
| US3828840A (en) | Cyclicly-operable machine adapted to produce and assemble cope and drag mold parts | |
| EP0035568A1 (de) | Ziegelsteinformmaschine | |
| US5362434A (en) | Vertical press and process for operating the same | |
| HUT72286A (en) | Device for transporting moulds | |
| GB2124541A (en) | Mechanism for exchanging molding dies in an injection molding machine | |
| JP2000071220A (ja) | レンガプレス装置 | |
| JPS6338072Y2 (de) | ||
| CN210023531U (zh) | 一种五金模具自动上料设备 | |
| EP0108148B1 (de) | Fülltisch in der giesstation einer giesserei | |
| KR100278088B1 (ko) | 조립식 타일블럭의 제조방법 및 장치 | |
| EP0468577B1 (de) | Anlage mit hoher Produktivität zur Herstellung von Keramikfliesen im allgemeinen | |
| US3318365A (en) | Apparatus for producing half molds by pressing | |
| CN119140819B (zh) | 一种粉末冶金设备 | |
| CN214976953U (zh) | 厨房推车储物盒成型专机 | |
| JPS5941081Y2 (ja) | 射出成形機の金型取付装置 | |
| GB1101530A (en) | Improvements in or relating to moulding machines | |
| US2511079A (en) | Molding apparatus | |
| SU1014649A1 (ru) | Установка дл выбивки литейных форм | |
| SU1088881A1 (ru) | Устройство дл заполнени пресс-формы порошком | |
| SU753644A1 (ru) | Устройство дл прессовани изделий из порошков | |
| JPS5941073Y2 (ja) | 射出成形機の金型取付装置 | |
| SU1291600A1 (ru) | Устройство дл формовани туалетного мыла | |
| SU733986A1 (ru) | Устройство дл формовани изделий |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): DE GB |
|
| 17P | Request for examination filed |
Effective date: 19810428 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Designated state(s): DE GB |
|
| REF | Corresponds to: |
Ref document number: 2966698 Country of ref document: DE Date of ref document: 19840322 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19961211 Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19961231 Year of fee payment: 18 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19971224 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19971224 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980901 |