EP0105841A1 - Werkstreifen zur Herstellung von Komponententrägern für Uhren - Google Patents
Werkstreifen zur Herstellung von Komponententrägern für Uhren Download PDFInfo
- Publication number
- EP0105841A1 EP0105841A1 EP83810436A EP83810436A EP0105841A1 EP 0105841 A1 EP0105841 A1 EP 0105841A1 EP 83810436 A EP83810436 A EP 83810436A EP 83810436 A EP83810436 A EP 83810436A EP 0105841 A1 EP0105841 A1 EP 0105841A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- grid
- network
- supports
- cutouts
- cuts
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 238000004519 manufacturing process Methods 0.000 title claims description 11
- 229910052751 metal Inorganic materials 0.000 claims description 7
- 239000002184 metal Substances 0.000 claims description 7
- 238000005520 cutting process Methods 0.000 claims description 5
- 239000006223 plastic coating Substances 0.000 claims 2
- BASFCYQUMIYNBI-UHFFFAOYSA-N platinum Chemical compound [Pt] BASFCYQUMIYNBI-UHFFFAOYSA-N 0.000 description 6
- 238000002347 injection Methods 0.000 description 5
- 239000007924 injection Substances 0.000 description 5
- 239000000243 solution Substances 0.000 description 5
- 239000000463 material Substances 0.000 description 3
- 238000000465 moulding Methods 0.000 description 3
- 239000011248 coating agent Substances 0.000 description 2
- 238000000576 coating method Methods 0.000 description 2
- 229910052697 platinum Inorganic materials 0.000 description 2
- 230000006866 deterioration Effects 0.000 description 1
- 230000004069 differentiation Effects 0.000 description 1
- 239000003365 glass fiber Substances 0.000 description 1
- 230000005226 mechanical processes and functions Effects 0.000 description 1
- MOFOBJHOKRNACT-UHFFFAOYSA-N nickel silver Chemical compound [Ni].[Ag] MOFOBJHOKRNACT-UHFFFAOYSA-N 0.000 description 1
- 239000010956 nickel silver Substances 0.000 description 1
- 125000000843 phenylene group Chemical group C1(=C(C=CC=C1)*)* 0.000 description 1
- 229920001021 polysulfide Polymers 0.000 description 1
- 230000000750 progressive effect Effects 0.000 description 1
- 239000010453 quartz Substances 0.000 description 1
- 230000002787 reinforcement Effects 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
- VYPSYNLAJGMNEJ-UHFFFAOYSA-N silicon dioxide Inorganic materials O=[Si]=O VYPSYNLAJGMNEJ-UHFFFAOYSA-N 0.000 description 1
- 239000010935 stainless steel Substances 0.000 description 1
- 229910001220 stainless steel Inorganic materials 0.000 description 1
- 239000000758 substrate Substances 0.000 description 1
Images


Classifications
-
- G—PHYSICS
- G04—HOROLOGY
- G04C—ELECTROMECHANICAL CLOCKS OR WATCHES
- G04C3/00—Electromechanical clocks or watches independent of other time-pieces and in which the movement is maintained by electric means
- G04C3/008—Mounting, assembling of components
-
- G—PHYSICS
- G04—HOROLOGY
- G04B—MECHANICALLY-DRIVEN CLOCKS OR WATCHES; MECHANICAL PARTS OF CLOCKS OR WATCHES IN GENERAL; TIME PIECES USING THE POSITION OF THE SUN, MOON OR STARS
- G04B29/00—Frameworks
- G04B29/02—Plates; Bridges; Cocks
- G04B29/027—Materials and manufacturing
Definitions
- the subject of the present invention is a working strip intended for the production of component support for a watch, by overmolding a metal grid cut from a metal strip.
- the object of the present invention is to provide a solution which does not have this drawback. It is achieved thanks to the fact that the ribbon comprises a plurality of sets of cuts which each comprise a first and a second network of cuts, separated by isthmus.
- the first network delimits a first grid usable for the manufacture of supports of a first dimension.
- the second network of cutouts, practiced in the first grid delimits a second grid, usable for the manufacture of supports of a second dimension, smaller than the first.
- the isthmus constitute cutting points allowing, after overmolding, to extract the supports from the ribbon.
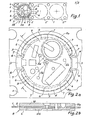
- the working strip shown in FIG. 1 comprises a metal strip 1 and, practiced in this strip, a plurality of sets of cuts 2, 2 ′, 2 ".
- Each set comprises first and second networks of cuts 3 and 4
- the cuts 3 of the first network are separated by isthmus 6, those 4 of the second network by isthmus 7.
- the first network of cuts 3 delimits a first grid 8, of generally circular shape, in which the second network of cuts 4 is practiced.
- the second network of cuts 4 delimits a second grid 9, also of generally circular shape, forming an integral part of the grid 8, but of smaller dimension.
- Each set of cuts further comprises a third network 5.
- the cutouts 5a define openings inside which will be housed the components of the watch (battery, quartz, motor, etc.). The role of the cutouts 5b will be defined later.
- the metal strip is advantageously made of stainless steel or nickel silver, the thickness of which is a few tenths of a millimeter (typically 0.3 mm).
- the cutting networks 3, 4 and 5 are produced by means of a press equipped with a progressive stamping.
- FIG. 2 represents an example of a large plate 11, produced by molding on the ribbon 1 of FIG. 1 a mass of plastic 10, coating the large grid 8, which extends to the level of the cutouts 3 It appears that the cutouts 5b make it possible to increase the adhesion of the plastic mass 10, thanks to the connections that they create between its upper part 10a and its lower part 10b.
- the internal dimension of the cutouts 3 is advantageously from 0.2 to 0.5 mm smaller than the external dimension of the plate 11. This gives good cohesion between the plastic material 10a of the upper part of the plate and the material 10b from the bottom.
- FIG. 3 represents an example of platinum 11, of small dimension, produced by molding on the ribbon 1 a mass of plastic 10 coating the small grid 9 and covering substantially the whole of the second network of cutouts 4.
- the difference in size between the two types of plates is insufficient to allow the injection mold to be closed in the space of the cutouts 4.
- the strip 1 is inserted therein and the size of the cuts 3 and 4 is chosen so that the periphery of the plate 11 (FIG. 3) is included in the interval which separates the cuts 3 from the cuts 4.
- the size of the platinum will preferably be equal to the external dimension of the cutouts 4. The mold comes to rest on part 8a of the grid 8, the latter thus participating in the definition of the injection volume.
- the plastic used can be a phenylene polysulphide supplemented with glass fibers.
- FIG. 4 differs from that of the preceding figures in that the larger plate is of round shape, that of smaller dimension of barrel shape.
- the parts 8a of the grid 8 do not have the shape of a crown sector, as is the case in FIG. 1, but of a crescent. This solution is advantageous for the manufacture of ladies' watches, with calendar when the round plate is used, without calendar in the case of the barrel plate.
- the grids 8 and 9 are primarily intended to stiffen the plate 11. It is obvious that they could also provide electrical connections between different components associated with the supports, or even include parts playing other mechanical functions, spring jumper or stack clamp for example.
- the working strip can not only be used as a support for the operations of molding the plate, but also for the operations of assembling the components.
- the separation of the plate and its support is obtained by cutting the isthmus 6 or 7 depending on whether it is a plate of larger or smaller dimension.
- This invention makes it possible to continuously manufacture identical strips for two different calibers, the differentiation only taking place during injection. This advantage is all the more significant since the injection operation is much slower than the cutting operation, a single press thus being able to serve several injection machines.
Landscapes
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Metallurgy (AREA)
- Slide Fasteners, Snap Fasteners, And Hook Fasteners (AREA)
- Punching Or Piercing (AREA)
- Casting Or Compression Moulding Of Plastics Or The Like (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CH584082 | 1982-10-05 | ||
| CH5840/82 | 1982-10-05 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP0105841A1 true EP0105841A1 (de) | 1984-04-18 |
Family
ID=4300173
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP83810436A Withdrawn EP0105841A1 (de) | 1982-10-05 | 1983-09-28 | Werkstreifen zur Herstellung von Komponententrägern für Uhren |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP0105841A1 (de) |
| JP (1) | JPS5999279A (de) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0321900A1 (de) * | 1987-12-23 | 1989-06-28 | Eta SA Fabriques d'Ebauches | Ein aus einem Streifenprofil hergestelltes Uhrenmittelteil |
| US5369627A (en) * | 1987-07-21 | 1994-11-29 | Seiko Epson Corporation | Improvements in bearing and frame structure of a timepiece |
| US5416752A (en) * | 1987-07-21 | 1995-05-16 | Seiko Epson Corporation | Timepiece |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH157097A (fr) * | 1931-03-30 | 1932-09-15 | Leon Levy & Freres Sa | Procédé de fabrication de plusieurs pièces métalliques de forme non régulière. |
| US3697816A (en) * | 1969-07-05 | 1972-10-10 | Bernhard Beyschlag Apparatebau | Electric network and method of making same |
| FR2356339A1 (fr) * | 1975-05-29 | 1978-01-20 | Texas Instruments Inc | Module electronique et son procede de fabrication |
-
1983
- 1983-09-28 EP EP83810436A patent/EP0105841A1/de not_active Withdrawn
- 1983-10-03 JP JP18325783A patent/JPS5999279A/ja active Pending
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH157097A (fr) * | 1931-03-30 | 1932-09-15 | Leon Levy & Freres Sa | Procédé de fabrication de plusieurs pièces métalliques de forme non régulière. |
| US3697816A (en) * | 1969-07-05 | 1972-10-10 | Bernhard Beyschlag Apparatebau | Electric network and method of making same |
| FR2356339A1 (fr) * | 1975-05-29 | 1978-01-20 | Texas Instruments Inc | Module electronique et son procede de fabrication |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5369627A (en) * | 1987-07-21 | 1994-11-29 | Seiko Epson Corporation | Improvements in bearing and frame structure of a timepiece |
| US5416752A (en) * | 1987-07-21 | 1995-05-16 | Seiko Epson Corporation | Timepiece |
| EP0321900A1 (de) * | 1987-12-23 | 1989-06-28 | Eta SA Fabriques d'Ebauches | Ein aus einem Streifenprofil hergestelltes Uhrenmittelteil |
| CH672225GA3 (de) * | 1987-12-23 | 1989-11-15 | ||
| US5077710A (en) * | 1987-12-23 | 1991-12-31 | Eta Sa Fabriques D'ebauches | Watchcase having caseband fashioned from a contoured strip |
Also Published As
| Publication number | Publication date |
|---|---|
| JPS5999279A (ja) | 1984-06-07 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA1114447A (fr) | Generateur electrochimique a electrolyte non aqueux | |
| EP0128822A1 (de) | Verfahren zur Herstellung von Speicherkarten und hierdurch hergestellte Karten | |
| EP0948064A1 (de) | Prismatische aufladbare oder primäre Zelle mit steifem und zusammendrückendem Halter | |
| FR2621180A1 (fr) | Borne de contact electrique de type cage | |
| EP1537630B1 (de) | Elektrischer anschlusskontakt mit elastischem kontaktblatt | |
| EP0198279B1 (de) | Modeartikel | |
| FR2487602A1 (fr) | Ensemble oscillateur piezo-electrique de type aplati ferme hermetiquement | |
| EP3958069A1 (de) | Armbanduhrgehäuse, das mit einem verkleidungselement ausgestattet ist | |
| EP2461220A1 (de) | Schallabstrahlungsmembran für eine Spieluhr oder eine Armbanduhr mit Schlagwerk | |
| FR2878653A1 (fr) | Antenne, montre munie de l'antenne, et procede de fabrication de l'antenne | |
| EP0024364A1 (de) | Vorrichtung zum Halten einer Batterie in einer elektronischen Armbanduhr | |
| EP0197416A1 (de) | Eine aus einem Uhrengehäuseteil und aus einem Armband gebildete Einheit sowie Herstellungsverfahren hierzu | |
| FR3088658A1 (fr) | Structure constituant un isolant acoustique | |
| EP0994398B1 (de) | Verfahren zur Herstellung eines Zahnrades für eine Uhr sowie ein nach diesem Verfahren hergestelltes Zahnrad | |
| FR2650116A1 (fr) | Interrupteur a bouton-poussoir | |
| WO1998045805A1 (fr) | Procede d'insertion d'un module electronique dans un corps de carte a memoire electronique | |
| EP0739064A1 (de) | Herstellungsverfahren für modulare Verbindereinheit und für die so erhaltene elektrische Verbindung | |
| WO2002082587A1 (fr) | Connecteur pour montage en surface de circuit imprime et procede de fabrication | |
| EP0089269B2 (de) | Schneckenhausförmiges Gefäss und Gussform zu seiner Herstellung | |
| EP1515203A1 (de) | Verfahren zur Produktion und zur Montage von elektrischen Kontakten für zerbrechliche Schalter, die in Uhrmacherei benutzt werden | |
| WO2014106656A1 (fr) | Procede de fabrication de batteries de type lithium-ion | |
| EP0131328B1 (de) | Sende-Empfangseinrichtung für ein Radar zur Anwesenheitswahrnehmung und Verfahren zur Herstellung | |
| EP0469970A1 (de) | Verfahren zur Herstellung einer Mikroschaltungskarte und dadurch erhaltene Karte | |
| EP0800426B1 (de) | Verfahren zur herstellung von flachen werkstücken und durch dieses verfahren hergestellte flache werkstücke | |
| CN113042973A (zh) | 一种光伏组件焊带现压扁工艺焊接方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): DE FR GB |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 19841219 |
|
| ITF | It: translation for a ep patent filed | ||
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: MEYRAT, CLEMENT |