EP0110127B1 - Procédé pour fabriquer un anneau de cuvelage pour commutateur - Google Patents
Procédé pour fabriquer un anneau de cuvelage pour commutateur Download PDFInfo
- Publication number
- EP0110127B1 EP0110127B1 EP83110668A EP83110668A EP0110127B1 EP 0110127 B1 EP0110127 B1 EP 0110127B1 EP 83110668 A EP83110668 A EP 83110668A EP 83110668 A EP83110668 A EP 83110668A EP 0110127 B1 EP0110127 B1 EP 0110127B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- punch
- ring
- forming
- stamp
- blank
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired
Links
- 238000004519 manufacturing process Methods 0.000 title claims description 5
- 238000000034 method Methods 0.000 claims description 10
- 239000000463 material Substances 0.000 description 4
- 238000007493 shaping process Methods 0.000 description 4
- 230000015572 biosynthetic process Effects 0.000 description 3
- 238000004873 anchoring Methods 0.000 description 2
- 238000001125 extrusion Methods 0.000 description 2
- 239000002699 waste material Substances 0.000 description 2
- 241001430066 Anulocaulis Species 0.000 description 1
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 1
- 229910052802 copper Inorganic materials 0.000 description 1
- 239000010949 copper Substances 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 230000018109 developmental process Effects 0.000 description 1
- 239000011810 insulating material Substances 0.000 description 1
- 230000000717 retained effect Effects 0.000 description 1
- 230000007704 transition Effects 0.000 description 1
Images

Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01R—ELECTRICALLY-CONDUCTIVE CONNECTIONS; STRUCTURAL ASSOCIATIONS OF A PLURALITY OF MUTUALLY-INSULATED ELECTRICAL CONNECTING ELEMENTS; COUPLING DEVICES; CURRENT COLLECTORS
- H01R43/00—Apparatus or processes specially adapted for manufacturing, assembling, maintaining, or repairing of line connectors or current collectors or for joining electric conductors
- H01R43/06—Manufacture of commutators
- H01R43/08—Manufacture of commutators in which segments are not separated until after assembly
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21J—FORGING; HAMMERING; PRESSING METAL; RIVETING; FORGE FURNACES
- B21J5/00—Methods for forging, hammering, or pressing; Special equipment or accessories therefor
- B21J5/06—Methods for forging, hammering, or pressing; Special equipment or accessories therefor for performing particular operations
- B21J5/12—Forming profiles on internal or external surfaces
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21K—MAKING FORGED OR PRESSED METAL PRODUCTS, e.g. HORSE-SHOES, RIVETS, BOLTS OR WHEELS
- B21K1/00—Making machine elements
- B21K1/28—Making machine elements wheels; discs
- B21K1/30—Making machine elements wheels; discs with gear-teeth
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21K—MAKING FORGED OR PRESSED METAL PRODUCTS, e.g. HORSE-SHOES, RIVETS, BOLTS OR WHEELS
- B21K1/00—Making machine elements
- B21K1/76—Making machine elements elements not mentioned in one of the preceding groups
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49002—Electrical device making
- Y10T29/49009—Dynamoelectric machine
- Y10T29/49011—Commutator or slip ring assembly
Definitions
- the invention is based on a method for producing a commutator segment ring according to the preamble of the main claim.
- a method for producing a commutator segment ring with a flange at one end is already known, in which a tool for cold forming is used.
- a ridge similar to an inner ring shoulder is formed on the end face of the flange which extends radially into the interior of the commutator segment ring.
- the shaping punch arranged on the end face of the upper punch is fastened with a screw which, even with the largest possible shaft diameter, cannot prevent the formation of the burr on the commutator segment ring.
- the larger the shank diameter of the screw the more the pressure stability of the die and thus the life of the forming tool is reduced.
- DE-A1-2544325 only discloses a method for forming axial inner ribs in a sleeve-shaped blank.
- the commutator segment ring thus formed without a flange has retained the length of the blank. Because when the blank is deformed, the inner ribs are essentially formed by a radial flow of material.
- the forming die forming the inner ribs is in one piece and longer than the workpiece and thus as the commutator segment ring, so that no burrs similar to inner ring shoulders can arise between the inner ribs on its end faces.
- the forming forces that only act on the blank to form the inner ribs are significantly lower than those required to form a ring into a commutator segment ring with a flange and a shaft length that is a multiple of the height of the ring.
- the invention has for its object to provide a method for producing a commutator segment ring of the type mentioned, in which the formation of a burr between the inner ribs, especially on the end face of the flange, is prevented with simple means.
- an elastic, force-adjustable countermeasure which counteracts the movement of the punch during the forming process, lies directly pressure-tight on the die and also presses the die against the top punch so that the formation of burrs on the end faces, especially on the the flange of the commutator segment ring is prevented and the commutator segment ring can be produced without waste and expensive rework.
- the elastic counter-support which supports the pressure tightness on the die, enables the use of a screw with a much smaller shaft diameter for fastening the die, thereby increasing the pressure stability and thus the service life of the die.
- the counter-punch serves as an ejector on the return stroke to its starting position and brings the shaped commutator segment ring into its removal position.
- FIG. 1 shows a blank for a commutator segment ring in longitudinal section
- FIG. 2 shows a commutator segment ring in longitudinal section
- FIG. 3 shows the commutator segment ring in partial cross section along line 111-111 in FIG. 2
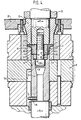
- FIG. 4 shows an exemplary embodiment of a forming tool at the end of the working stroke in longitudinal section.
- a blank 1 for a commutator segment ring 2 of a commutator is made of a material suitable for commutators, for example copper.
- the blank 1 has the shape of a ring with a rectangular or round cross section.
- the blank 1 can be a section of a hollow cylinder.
- the blank 1 can be formed from a strand section which is bent into a ring.
- a shaft 3 with a flange 4 is formed from the ring-shaped blank 1, a plurality of axial inner ribs being formed at the same distance from one another by means of a stamp on the inside of the shaft 3 of the blank 1 are arranged.
- the inner ribs form the starting form for commutator segments 5, which are separated from one another by segment partial grooves 6 and are only connected by narrow webs 7.
- the webs 7 can also be curved outwards in order to reduce the amount of material required for the commutator segment ring 2.
- the blank 1 can be compressed in a subsequent reduction stage which is known per se and is not shown in detail, the webs 7 arching outwards.
- the cold forming of the blank 1 in the commutator segment ring 2 takes place in a multi-part forming tool in one working stroke.
- FIG. 4 An embodiment of the forming tool is shown in Figure 4 in the position at the end of the working stroke.
- a longitudinal bore 9 is formed with an enlarged receiving section 10.
- a hollow cylindrical extrusion die 11 is inserted, the inner shape of which corresponds to the outer shape of the commutator segment ring to be formed.
- a guide slot 12 is formed in the longitudinal bore 9.
- a lower punch 13 is guided to be longitudinally movable.
- a pin 14 arranged radially in the punch 13 protrudes into the guide slot 12 as an embodiment of a rotation lock and limitation of the longitudinal movement of the lower punch 13.
- the punch 13 can also be used by known and not shown limiting and guiding means of the control and / or actuating device of the forming tool or rotational and longitudinal direction-securing components in its position and limited in its movement.
- the control stamp 16 rests with its other end in a manner known per se and not shown in more detail on an elastic control means, for example a hydraulic counterhold or a gas spring.
- the upper end face 17 of the lower punch 13 is provided with a coaxial recess 18 with a shoulder 19.
- the depression 18 can also be designed as a continuous longitudinal bore.
- a ring stamp 21 is fastened in a central stamp plate 20, which is movable relative to the lower stamp plate 8. Its outer diameter corresponds to the diameter of the receiving section 10 in the lower stamp plate 8.
- an upper stamp 22 is guided in a longitudinally movable manner and is received in an upper stamp plate 23.
- the middle and the upper stamp plate 20 and 23 are movable with each other and relative to each other.
- a shaping punch 25 is arranged on the front face 24 of the upper punch 22.
- the shaping stamp 25 is provided on its circumference with teeth 26 formed on it at the same angular distance from one another, the profile of which corresponds to the segment grooves 6 of the commutator ring 2.
- a pressure ring 28 On the end face 27 of the forming punch 25 facing away from the upper punch 22, there is a pressure ring 28, the outside diameter of which is somewhat smaller than the diameter of the tooth base circle of the forming punch 25. With a screw 29, the head of which rests on the pressure ring 28, the forming punch 25 together with the pressure ring is 28 attached to the end face 24 of the upper punch 22.
- the use of the pressure ring 28 contributes to enabling a largely pressure-tight attachment of the die 25 with a screw 29 of relatively small diameter.
- the thinner screw 29 increases the service life of the die, since the die cross section can remain comparatively large and thus has a large counterpressure receiving area.
- the die 11 inserted into the receiving section 10 of the lower holding plate 8 has an inwardly slightly conical end face 30.
- the transition between the end face 30 and the central bore of the die 11 is designed as a chamfer 31.
- the middle and the upper stamp plate 20 and 23 with the ring stamp 21 and the upper stamp 22 together with the form stamp 25 are lifted off the lower stamp plate 8 and held in their uppermost position.
- the upper stamp 22 is retracted far into the ring stamp 21.
- the lower punch 13 is pushed so far into the die 11 by the control punch 16 that its end face 17 borders on the end face 30 of the die 11.
- the blank 1 is inserted into the receiving section 10 of the lower punch plate 8 so that it lies on the end face 30 of the die 11 which forms the workpiece holder.
- the middle and the upper stamp plates 20 and 23 with the ring stamp 21 and the upper stamp 22 with the form stamp 25 are first moved towards the blank 1. If the ring stamp 21 now guided in the receiving section 10 rests on the blank 1, the upper stamp 22 with the form stamp 25 is moved further into the blank 1 until the Form stamp 25 with its face on the end face 24 of the upper stamp 22 lying in a pressure-tight manner lies in one plane with the end face of the ring stamp 21. The upper stamp plate 23 then lies on the ring stamp 21 on the middle stamp plate 20.
- the die 25 hits the lower die 13 during movement through the blank 1 into the die 11 or with the pressure ring 28, it presses it correspondingly far against the force of the control die 16 supported on the adjustable elastic control means out of the die 11 into the longitudinal bore 9 of the lower holding plate 8.
- the stamp plates 20 and 23 with ring stamp 21 and upper stamp 22 with form stamp 25 and pressure ring 28 are then moved on together.
- the ring stem 21 now forms the flange 4.
- the displaced material of the blank 10 is extruded into the shaft 3 with commutator segments 5 forming between the teeth 26 of the die 25 and webs 7 forming between the inner wall of the die 11 and the outside of the teeth 26.
- the lower punch 13 also forms the limitation of the length of the shaft 3 on the end of the commutator segment ring 2 facing away from the flange 4. At the end of the working stroke for shaping the blank 1 into the commutator segment ring 2, the middle stamp plate 20 rests on the lower stamp plate 8.
- the commutator segment ring 2 can now be provided with anchoring means and an insulating material hub, in which the commutator segments 5 are anchored, in a manner known per se and not shown in detail. Likewise, the commutator segments 5 are then separated by removing the webs 7 and connecting lugs formed in the flange 4 are provided with flag slots, and the commutator is thus completed.
- the commutator segment ring 2 can be formed from the blank 1 both by forward and backward extrusion.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Motor Or Generator Current Collectors (AREA)
- Manufacture Of Motors, Generators (AREA)
- Manufacturing Of Electrical Connectors (AREA)
Claims (3)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3242702 | 1982-11-19 | ||
| DE19823242702 DE3242702A1 (de) | 1982-11-19 | 1982-11-19 | Verfahren zum herstellen eines kommutatorsegmentringes |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0110127A1 EP0110127A1 (fr) | 1984-06-13 |
| EP0110127B1 true EP0110127B1 (fr) | 1987-07-01 |
Family
ID=6178452
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP83110668A Expired EP0110127B1 (fr) | 1982-11-19 | 1983-10-26 | Procédé pour fabriquer un anneau de cuvelage pour commutateur |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US4611391A (fr) |
| EP (1) | EP0110127B1 (fr) |
| JP (1) | JPS59103541A (fr) |
| DE (2) | DE3242702A1 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4313712A1 (de) * | 1993-04-27 | 1994-11-03 | Gkn Automotive Ag | Verfahren und Vorrichtung zur Anbringung einer Profilverzahnung auf einer Welle |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5765425A (en) * | 1993-05-17 | 1998-06-16 | Pipan; Janez | Radial extrusion process combined with inside tune ironing |
| US5492001A (en) * | 1994-01-18 | 1996-02-20 | Kabushiki Kaisha Yutaka Giken | Method and apparatus for working burred portion of workpiece |
| WO1995022184A1 (fr) * | 1994-02-10 | 1995-08-17 | Comtrade Handelsgesellschaft Mbh | Bague d'armature pour corps de rotation et son procede de fabrication |
| JP2847093B2 (ja) * | 1996-03-11 | 1999-01-13 | ソニー株式会社 | ビデオカメラ |
| CN103801650A (zh) * | 2012-11-07 | 2014-05-21 | 四川众友机械有限责任公司 | 双联直齿圆柱齿轮齿形精密锻造工艺 |
| JP5884800B2 (ja) * | 2013-09-18 | 2016-03-15 | トヨタ自動車株式会社 | センター孔形成方法及び鍛造装置 |
| CN106077396B (zh) * | 2016-08-23 | 2018-12-25 | 合肥学院 | 圆柱直齿轮真空热精锻成形模具及加工方法 |
Family Cites Families (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3423819A (en) * | 1966-12-12 | 1969-01-28 | Ford Motor Co | Method of forming relatively straight lengths of metal into elongated members |
| US3608350A (en) * | 1969-03-04 | 1971-09-28 | Terumoto Yamaguchi | Apparatus and method for producing blanks for commutators for miniature electric devices |
| JPS4837761B1 (fr) * | 1969-06-13 | 1973-11-13 | ||
| DE1934213C3 (de) * | 1969-07-05 | 1980-07-10 | Robert Bosch Gmbh, 7000 Stuttgart | Verfahren zur Herstellung eines Kommutators |
| DE2064638A1 (de) * | 1970-12-31 | 1972-07-13 | Zahnradfabrik Friedrichshafen Ag, 7990 Friedrichshafen | Spanlose Fertigung von Mitnehmerringen |
| US3768295A (en) * | 1972-02-08 | 1973-10-30 | Reynolds Metals Co | Forming apparatus and method |
| JPS5017353A (fr) * | 1973-06-19 | 1975-02-24 | ||
| JPS585515B2 (ja) * | 1974-03-13 | 1983-01-31 | 株式会社デンソー | カイテンデンキヨウセイリユウシノ セイゾウホウホウ |
| JPS5939533B2 (ja) * | 1975-08-16 | 1984-09-25 | イケダ ツギノブ | 並列糸分離方法 |
| DE2544325C2 (de) * | 1975-10-03 | 1985-01-31 | Hitachi, Ltd., Tokio/Tokyo | Vorrichtung zum Herstellen eines zylindrischen ringförmigen Werkstückes mit an seinem Innenumfang angeordneten Zähnen |
| US4299112A (en) * | 1977-10-20 | 1981-11-10 | Kabushiki Kaisha Wako | Method and device for producing synchronizer ring |
| DE3203438A1 (de) * | 1982-02-02 | 1983-08-11 | Motomak Motorenbau, Maschinen- u. Werkzeugfabrik, Konstruktionen GmbH, 8070 Ingolstadt | Verfahren zur herstellung einer metallmuffe aus einem zylindrischen rohrabschnitt |
| US4463590A (en) * | 1982-02-25 | 1984-08-07 | The Harris-Thomas Drop Forge Company | Forging method |
| JPS58157521A (ja) * | 1982-03-16 | 1983-09-19 | Nissan Motor Co Ltd | 歯車製造方法および歯車製造装置 |
-
1982
- 1982-11-19 DE DE19823242702 patent/DE3242702A1/de not_active Withdrawn
-
1983
- 1983-10-26 DE DE8383110668T patent/DE3372260D1/de not_active Expired
- 1983-10-26 EP EP83110668A patent/EP0110127B1/fr not_active Expired
- 1983-11-17 US US06/552,984 patent/US4611391A/en not_active Expired - Fee Related
- 1983-11-18 JP JP58216396A patent/JPS59103541A/ja active Pending
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4313712A1 (de) * | 1993-04-27 | 1994-11-03 | Gkn Automotive Ag | Verfahren und Vorrichtung zur Anbringung einer Profilverzahnung auf einer Welle |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0110127A1 (fr) | 1984-06-13 |
| DE3242702A1 (de) | 1984-05-24 |
| JPS59103541A (ja) | 1984-06-15 |
| DE3372260D1 (en) | 1987-08-06 |
| US4611391A (en) | 1986-09-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0761336B1 (fr) | Méthode et appareil de fabrication d'un collecteur | |
| DE69301123T2 (de) | Ventilführungseinsatz | |
| DE2747382C2 (de) | Verfahren zur Herstellung eines einen hohlzylindrischen Teil aufweisenden Flanschstückes und Vorrichtung zur Durchführung des Verfahrens | |
| DE1259182B (de) | Vorrichtung zum Kaltpressen doppelnapffoermiger Zuendkerzengehaeuse | |
| EP0748942A1 (fr) | Système de fixation et procédé pour fixer deux pièces de façon détachable | |
| WO1999049227A2 (fr) | Procede, outil et poinçon pour relier des composants a une plaque | |
| EP2760605B1 (fr) | Procédé et dispositif de fabrication d'un pignon récepteur à denture basse | |
| DE1750019A1 (de) | Hohlbolzen und Verfahren zu seiner Herstellung | |
| DE112014004712T5 (de) | Herstellungsverfahren für einen geformten Primär-Metallpassteil-Gegenstand für eine Zündkerze, Herstellungsverfahren für ein Primär-Metallpassteil für eine Zündkerze und Zündkerzen-Herstellverfahren | |
| DE2226070B2 (de) | Kupplungshülse zum Verbinden von elektrischen Leitern und Verfahren zu deren Herstellung | |
| DE3610675C2 (de) | Verfahren und Vorrichtung zum Anbringen eines Hohlkörpers an einem tafelförmigen Werkstück | |
| EP0111687B1 (fr) | Méthode de fabrication d'une bague de segments de commutateur | |
| EP0110127A1 (fr) | Procédé pour fabriquer un anneau de cuvelage pour commutateur | |
| EP3639947B1 (fr) | Procédé et dispositif de fabrication d'un élément de raccordement | |
| EP0111688B1 (fr) | Méthode de fabrication d'une bague de commutateur pour un commutateur | |
| EP0085388B1 (fr) | Procédé de fabrication d'un manchon métallique à partir d'une pièce tubulaire cylindrique | |
| EP0137957B1 (fr) | Procédé pour fabriquer un étage intermédiaire pour un cône mobile de lame de collecteur | |
| EP1355749A1 (fr) | Procede de montage d'un element de fonction sur une piece de metal deformable a l'aide d'un procede de formage sous haute pression, piece assemblee et matrice | |
| EP1591676B1 (fr) | Elément rapporté à enfoncement automatique pour tôle | |
| DE10309381A1 (de) | Verfahren zum Verbinden zweier Werksücke in einem Fügebereich | |
| DE3201027C2 (de) | Verfahren zum Herstellen eines Kommutatorringes | |
| DE10153224B4 (de) | Verfahren und Vorrichtung zum Formen und/oder Beschneiden eines Hohlkörpers aus einem Hohlprofil od.dgl. Werkstück | |
| DE102008039685A1 (de) | Verfahren zur Herstellung einer Hülse mit Blindnuten, die als Ölreservoir für eine Kette dienen | |
| EP1572394B1 (fr) | Bouchon a vis metallique, procede pour le produire, ebauche utilisee a cette fin et outil correspondant | |
| EP1250199B1 (fr) | Procede et outil de deformation pour la fabrication de tubes cylindriques par formage par fluage |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19831026 |
|
| AK | Designated contracting states |
Designated state(s): DE FR GB |
|
| 17Q | First examination report despatched |
Effective date: 19860319 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB |
|
| REF | Corresponds to: |
Ref document number: 3372260 Country of ref document: DE Date of ref document: 19870806 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19901227 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19911015 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19911030 Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19920701 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19921026 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19921026 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19930630 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |