EP0111449A2 - Verfahren zur Herstellung eines äusseren Uhrenteils und durch dieses Verfahren hergestelltes Teil - Google Patents
Verfahren zur Herstellung eines äusseren Uhrenteils und durch dieses Verfahren hergestelltes Teil Download PDFInfo
- Publication number
- EP0111449A2 EP0111449A2 EP83810564A EP83810564A EP0111449A2 EP 0111449 A2 EP0111449 A2 EP 0111449A2 EP 83810564 A EP83810564 A EP 83810564A EP 83810564 A EP83810564 A EP 83810564A EP 0111449 A2 EP0111449 A2 EP 0111449A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- watch case
- fixing member
- element according
- case element
- crystal
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 9
- 238000000034 method Methods 0.000 title claims description 10
- 239000011521 glass Substances 0.000 claims abstract description 17
- 239000000463 material Substances 0.000 claims abstract description 17
- 238000000576 coating method Methods 0.000 claims abstract description 13
- 239000011248 coating agent Substances 0.000 claims abstract description 10
- 239000013078 crystal Substances 0.000 claims abstract description 9
- 238000000465 moulding Methods 0.000 claims abstract description 7
- 239000012768 molten material Substances 0.000 claims abstract description 5
- 238000004873 anchoring Methods 0.000 claims description 3
- 230000002093 peripheral effect Effects 0.000 claims description 3
- 239000007769 metal material Substances 0.000 claims description 2
- 239000011368 organic material Substances 0.000 claims description 2
- 229910052751 metal Inorganic materials 0.000 description 6
- 239000002184 metal Substances 0.000 description 6
- PCHJSUWPFVWCPO-UHFFFAOYSA-N gold Chemical compound [Au] PCHJSUWPFVWCPO-UHFFFAOYSA-N 0.000 description 4
- 229910052737 gold Inorganic materials 0.000 description 4
- 239000010931 gold Substances 0.000 description 4
- 239000000470 constituent Substances 0.000 description 3
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 2
- ATJFFYVFTNAWJD-UHFFFAOYSA-N Tin Chemical compound [Sn] ATJFFYVFTNAWJD-UHFFFAOYSA-N 0.000 description 2
- 229910000842 Zamak Inorganic materials 0.000 description 2
- HCHKCACWOHOZIP-UHFFFAOYSA-N Zinc Chemical compound [Zn] HCHKCACWOHOZIP-UHFFFAOYSA-N 0.000 description 2
- 229910045601 alloy Inorganic materials 0.000 description 2
- 239000000956 alloy Substances 0.000 description 2
- 229910052802 copper Inorganic materials 0.000 description 2
- 239000010949 copper Substances 0.000 description 2
- 238000002347 injection Methods 0.000 description 2
- 239000007924 injection Substances 0.000 description 2
- 230000000873 masking effect Effects 0.000 description 2
- 238000001465 metallisation Methods 0.000 description 2
- 229910052718 tin Inorganic materials 0.000 description 2
- 229910052725 zinc Inorganic materials 0.000 description 2
- 239000011701 zinc Substances 0.000 description 2
- WKVZMKDXJFCMMD-UVWUDEKDSA-L (5ar,8ar,9r)-5-[[(2r,4ar,6r,7r,8r,8as)-7,8-dihydroxy-2-methyl-4,4a,6,7,8,8a-hexahydropyrano[3,2-d][1,3]dioxin-6-yl]oxy]-9-(4-hydroxy-3,5-dimethoxyphenyl)-5a,6,8a,9-tetrahydro-5h-[2]benzofuro[6,5-f][1,3]benzodioxol-8-one;azanide;n,3-bis(2-chloroethyl)-2-ox Chemical compound [NH2-].[NH2-].Cl[Pt+2]Cl.ClCCNP1(=O)OCCCN1CCCl.COC1=C(O)C(OC)=CC([C@@H]2C3=CC=4OCOC=4C=C3C(O[C@H]3[C@@H]([C@@H](O)[C@@H]4O[C@H](C)OC[C@H]4O3)O)[C@@H]3[C@@H]2C(OC3)=O)=C1 WKVZMKDXJFCMMD-UVWUDEKDSA-L 0.000 description 1
- 229910000906 Bronze Inorganic materials 0.000 description 1
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 description 1
- FYYHWMGAXLPEAU-UHFFFAOYSA-N Magnesium Chemical compound [Mg] FYYHWMGAXLPEAU-UHFFFAOYSA-N 0.000 description 1
- 229910000831 Steel Inorganic materials 0.000 description 1
- 229910001297 Zn alloy Inorganic materials 0.000 description 1
- 238000004026 adhesive bonding Methods 0.000 description 1
- 229910052782 aluminium Inorganic materials 0.000 description 1
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 1
- 238000000429 assembly Methods 0.000 description 1
- 230000000712 assembly Effects 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000010974 bronze Substances 0.000 description 1
- 238000005119 centrifugation Methods 0.000 description 1
- 229910052804 chromium Inorganic materials 0.000 description 1
- 239000011651 chromium Substances 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 238000001816 cooling Methods 0.000 description 1
- KUNSUQLRTQLHQQ-UHFFFAOYSA-N copper tin Chemical compound [Cu].[Sn] KUNSUQLRTQLHQQ-UHFFFAOYSA-N 0.000 description 1
- 238000000151 deposition Methods 0.000 description 1
- 230000008021 deposition Effects 0.000 description 1
- 239000006023 eutectic alloy Substances 0.000 description 1
- 230000005496 eutectics Effects 0.000 description 1
- 230000004927 fusion Effects 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 230000007774 longterm Effects 0.000 description 1
- 238000003754 machining Methods 0.000 description 1
- 229910052749 magnesium Inorganic materials 0.000 description 1
- 239000011777 magnesium Substances 0.000 description 1
- 230000008018 melting Effects 0.000 description 1
- 238000002844 melting Methods 0.000 description 1
- 229910001092 metal group alloy Inorganic materials 0.000 description 1
- 239000000203 mixture Substances 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 229920003023 plastic Polymers 0.000 description 1
- 239000010970 precious metal Substances 0.000 description 1
- 230000001681 protective effect Effects 0.000 description 1
- 238000010079 rubber tapping Methods 0.000 description 1
- 229910052594 sapphire Inorganic materials 0.000 description 1
- 239000010980 sapphire Substances 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
- 238000007711 solidification Methods 0.000 description 1
- 230000008023 solidification Effects 0.000 description 1
- 239000000243 solution Substances 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
- 239000011135 tin Substances 0.000 description 1
Images
Classifications
-
- G—PHYSICS
- G04—HOROLOGY
- G04B—MECHANICALLY-DRIVEN CLOCKS OR WATCHES; MECHANICAL PARTS OF CLOCKS OR WATCHES IN GENERAL; TIME PIECES USING THE POSITION OF THE SUN, MOON OR STARS
- G04B39/00—Watch crystals; Fastening or sealing of crystals; Clock glasses
- G04B39/02—Sealing crystals or glasses
- G04B39/025—Sealing crystals or glasses without special sealing parts
-
- G—PHYSICS
- G04—HOROLOGY
- G04B—MECHANICALLY-DRIVEN CLOCKS OR WATCHES; MECHANICAL PARTS OF CLOCKS OR WATCHES IN GENERAL; TIME PIECES USING THE POSITION OF THE SUN, MOON OR STARS
- G04B37/00—Cases
- G04B37/22—Materials or processes of manufacturing pocket watch or wrist watch cases
-
- G—PHYSICS
- G04—HOROLOGY
- G04B—MECHANICALLY-DRIVEN CLOCKS OR WATCHES; MECHANICAL PARTS OF CLOCKS OR WATCHES IN GENERAL; TIME PIECES USING THE POSITION OF THE SUN, MOON OR STARS
- G04B39/00—Watch crystals; Fastening or sealing of crystals; Clock glasses
-
- G—PHYSICS
- G04—HOROLOGY
- G04B—MECHANICALLY-DRIVEN CLOCKS OR WATCHES; MECHANICAL PARTS OF CLOCKS OR WATCHES IN GENERAL; TIME PIECES USING THE POSITION OF THE SUN, MOON OR STARS
- G04B39/00—Watch crystals; Fastening or sealing of crystals; Clock glasses
- G04B39/02—Sealing crystals or glasses
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/49—Method of mechanical manufacture
- Y10T29/49579—Watch or clock making
- Y10T29/49584—Watch or clock making having case, cover, or back
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T29/00—Metal working
- Y10T29/53—Means to assemble or disassemble
- Y10T29/5347—Crystal to watch or clock
Definitions
- the present invention relates to the assembly of the constituent elements of a watch case and it relates more particularly to a method for manufacturing a watch case element comprising on the one hand a crystal, and on the other hand a rigidly secured fixing member to the latter, as well as the element obtained by this process and a watch case comprising this element.
- the present invention proposes a new method for producing a watch case element comprising a crystal and a fixing member subject to the latter, which allows. an easy realization of this fixing member, in various materials, which are themselves easy to machine if necessary, and this in any desired form.
- the latter also proposes watch case elements manufactured according to the aforementioned process, as well as a watch case incorporating them.
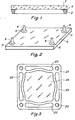
- a watch case element consists of a lens 1, to which a fixing member 2 is attached.
- a metal covering 3 is provided, the purpose of which is to ensure masking of the fastening member 2, and to guarantee better resistance of the assembly.
- the glass 1 can have any desired shape
- the fixing member 2, constituting an annular heel for fixing the glass can have a corresponding shape.
- this heel may not extend over the entire periphery of the glass, but only, for example, along two opposite sides of a glass of rectangular or square shape.
- FIG. 2 there is shown a glass 4, also provided with metal coating zones 5, at which are fixed fixing pads 6 extending perpendicular to the plane of the glass and forming fixing members.
- the fastening members 2 or 6 are not manufactured separately, then assembled with ice in an often imperfect manner, as in the prior art, but formed directly on the respective metallic coatings by a process for molding a molten material.
- the material of the fasteners is compatible with, and has a good affinity for the material of the metal coating, the choice of the material of the fasteners is wide, and most of the metal alloys commonly used in the watchmaking or precision mechanics can be used.
- the fixing members are made of a metal of the zinc, tin, copper, gold type, in the pure or alloyed state.
- the metal known under the name zamac which is an alloy of zinc, aluminum, copper and magnesium, or other types of alloys as well.
- Eutectic alloys are particularly interesting, since the eutectic composition of an alloy leads to a lower melting temperature.
- the coatings used at the junction between the connecting members and the glass panels can be deposited according to various known methods, such as for example by vacuum metallization or galvanic deposition.
- These coatings may have several layers, for example a chromium undercoat ensuring adhesion to the glass and masking of the fixing member, to which is superimposed a second layer of a material similar to that of the fixing members. to ensure the attachment of the metal during molding.
- a chromium undercoat ensuring adhesion to the glass and masking of the fixing member, to which is superimposed a second layer of a material similar to that of the fixing members. to ensure the attachment of the metal during molding.
- an outer layer of zinc will be used to secure a zamak fastener or gold to secure a gold fastener.
- a glass 20, 20 ′ is shown in view from below, provided with a peripheral heel 21, 21 ′ which has a variable width so as to be slightly deformable in a radial direction, for example for absorb the stresses during the cooling of the material forming the heel, or those due to differences in coefficients of thermal expansion between the ice and the heel.
- This variable width can be obtained by providing narrowing in the general shape of the heel, as well as openings 22 (fig. 3), or even by means of notches 22 '(fig. 4) left alternately on each lateral face of the heel. during molding. Taps 23, 23 'allow the member 21, 21' to be fixed in a watch case middle.
- FIG 5 another embodiment of a watch case element according to the invention has been shown.
- the fixing member 24 extends beyond the lateral edges of the glass 25, over at least part of its periphery.
- the member 24 extends in part at the height of these edges which it traps during the solidification of the constituent material and the volume shrinkage which accompanies it. A clamping by wedging and a tight connection of the glass 25 and the fixing member 24 can thus be obtained.
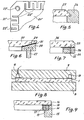
- FIG. 6 illustrates yet another variant of the invention, in which inserts 27, constituted for example by threaded steel studs, are partially embedded in a fixing member 28 at the time of its production, for allow it to be anchored in another element of a watch case. Furthermore, it can be seen that the fixing member 28 can be produced on an inclined lower part 29 of the lens 30, with the interposition of a coating 31.
- the fixing member 33 has two adjacent areas, separated by the dotted line 34 and made of different materials.
- a first layer adjacent to the coating 35 of the glass 36 can be made of tin to ensure good adhesion with the coating 35, while the zone situated below this layer can be made of a bronze having better qualities. mechanical.
- the line 34 does not correspond to an abrupt separation between the two zones, but to a region of interpenetration of the two neighboring materials.
- the external part of the fixing member 33 is provided with a cap 36 which can be made of a hard material, or of a precious metal such as gold. This cap, which can therefore have a protective or decorative function can be, for example, attached to the member 33 after its formation, or even already inside the mold used for the manufacture of this member.
- FIG. 8 is shown schematically an installation allowing the production of the watch case elements of FIGS. 1 or 2.
- the crystal 1 is placed between two parts 8, 9 of an injection mold, the part 9 comprising a channel 10 the shape of which corresponds to that of the fixing member to be formed.
- An opening 11 allows this channel to communicate with the outside and e fill with molten material.
- the ice 1) could be heated inside the mold, and all the methods: onnu of molding of molten material can be used, for example the injection under pressure by centrifugation, or the molding in a oven kept at low pressure, in order to lower the fusion joint of the materials used.
- FIG 9 there is shown another aspect of the invention, according to which a fixing member 13 produced as indicated above, is used not only to secure a lens 14 to the upper part of a component 15 of a watch case, such as a middle or a bezel, but also to ensure the watertightness of the assembly.
- the fixing member 13 the constituent material of which can be chosen so as to be able to closely match the external shape of a housing 16 formed in the part 15, is forcibly engaged in this housing, and its support on the lateral surface of the housing 16 is further improved .by a tension ring 17 disposed radially inside the annular fixing member 13.
- the metallization 18 of the underside of the glass is of course extends beyond the tension ring 17.
Landscapes
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- Chemical & Material Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Adornments (AREA)
- Joining Of Glass To Other Materials (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CH726282A CH650634GA3 (de) | 1982-12-14 | 1982-12-14 | |
| CH7262/82 | 1982-12-14 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0111449A2 true EP0111449A2 (de) | 1984-06-20 |
| EP0111449A3 EP0111449A3 (en) | 1984-07-18 |
| EP0111449B1 EP0111449B1 (de) | 1986-10-29 |
Family
ID=4322380
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP83810564A Expired EP0111449B1 (de) | 1982-12-14 | 1983-12-05 | Verfahren zur Herstellung eines äusseren Uhrenteils und durch dieses Verfahren hergestelltes Teil |
Country Status (7)
| Country | Link |
|---|---|
| US (1) | US4589886A (de) |
| EP (1) | EP0111449B1 (de) |
| JP (1) | JPS59120880A (de) |
| KR (1) | KR890000083B1 (de) |
| CH (1) | CH650634GA3 (de) |
| DE (1) | DE3367288D1 (de) |
| HK (1) | HK34992A (de) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4637734A (en) * | 1984-07-12 | 1987-01-20 | Montres Rado S.A. | Watch case |
| CH678680GA3 (en) * | 1990-02-20 | 1991-10-31 | Watch glass mounting - has a deposited metal layer between decorative layer and solder to prevent visible effects of soldering | |
| EP2261757A1 (de) | 2009-06-10 | 2010-12-15 | ETA SA Manufacture Horlogère Suisse | Verfahren und Vorrichtung zur Befestigung eines Glases an einem Glasreif |
| EP2595008A1 (de) * | 2011-11-17 | 2013-05-22 | Montres Rado S.A. | Gehäuse für eine Uhr |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5251846A (en) * | 1990-07-23 | 1993-10-12 | Vehicle Research Corporation | Supersonic aircraft shock wave energy recovery system |
| US7861966B2 (en) * | 2005-04-18 | 2011-01-04 | Vehicle Research Corporation | Supersonic aircraft footprint spreading control system and method |
| JP5824969B2 (ja) * | 2011-08-29 | 2015-12-02 | セイコーエプソン株式会社 | カバーガラスおよび時計 |
| JP6150407B1 (ja) * | 2016-03-08 | 2017-06-21 | セイコーインスツル株式会社 | 時計部品、文字板、文字板ユニット、ムーブメントおよび時計 |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH13597A (fr) * | 1896-11-27 | 1897-07-31 | Richard Lagerie Emile | Machine à étirer (peigner, carder, défeutrer) les matières textiles |
| US2468239A (en) * | 1943-11-18 | 1949-04-26 | Us Rubber Co | Method of bonding rubber to metal |
| US2597935A (en) * | 1946-04-22 | 1952-05-27 | Corning Glass Works | Cover glass assembly |
| US2854815A (en) * | 1954-09-24 | 1958-10-07 | Piquerez Ervin | Double watch crystal with moisture absorbent and indicating packing |
| CH317169A4 (de) * | 1969-03-03 | 1971-10-29 | ||
| FR2051627A1 (en) * | 1969-07-09 | 1971-04-09 | Chapuis Laurent | Wrist watch case construction |
| CH623711B (de) * | 1978-12-15 | Bbc Brown Boveri & Cie | Uhr. | |
| JPS5696267A (en) * | 1979-12-28 | 1981-08-04 | Seiko Epson Corp | Fixation of cover glass |
| CH649435GA3 (de) * | 1981-05-22 | 1985-05-31 | ||
| US4497584A (en) * | 1982-06-21 | 1985-02-05 | Firma H. Finger | Wrist watch case with vulcanized gasket |
-
1982
- 1982-12-14 CH CH726282A patent/CH650634GA3/fr unknown
-
1983
- 1983-11-16 KR KR1019830005433A patent/KR890000083B1/ko not_active Expired
- 1983-12-05 EP EP83810564A patent/EP0111449B1/de not_active Expired
- 1983-12-05 US US06/557,917 patent/US4589886A/en not_active Expired - Lifetime
- 1983-12-05 DE DE8383810564T patent/DE3367288D1/de not_active Expired
- 1983-12-12 JP JP58232889A patent/JPS59120880A/ja active Granted
-
1992
- 1992-05-14 HK HK349/92A patent/HK34992A/xx not_active IP Right Cessation
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4637734A (en) * | 1984-07-12 | 1987-01-20 | Montres Rado S.A. | Watch case |
| CH678680GA3 (en) * | 1990-02-20 | 1991-10-31 | Watch glass mounting - has a deposited metal layer between decorative layer and solder to prevent visible effects of soldering | |
| EP2261757A1 (de) | 2009-06-10 | 2010-12-15 | ETA SA Manufacture Horlogère Suisse | Verfahren und Vorrichtung zur Befestigung eines Glases an einem Glasreif |
| US8764283B2 (en) | 2009-06-10 | 2014-07-01 | Eta Sa Manufacture Horlogère Suisse | Process and device for fastening a glass to a bezel |
| EP2595008A1 (de) * | 2011-11-17 | 2013-05-22 | Montres Rado S.A. | Gehäuse für eine Uhr |
| WO2013072360A1 (fr) * | 2011-11-17 | 2013-05-23 | Montres Rado Sa | Boîte pour pièce d'horlogerie |
| US9164488B2 (en) | 2011-11-17 | 2015-10-20 | Montres Rado Sa | Case for a timepiece |
Also Published As
| Publication number | Publication date |
|---|---|
| KR890000083B1 (ko) | 1989-03-07 |
| HK34992A (en) | 1992-05-22 |
| JPH0253757B2 (de) | 1990-11-19 |
| CH650634GA3 (de) | 1985-08-15 |
| US4589886A (en) | 1986-05-20 |
| EP0111449A3 (en) | 1984-07-18 |
| DE3367288D1 (en) | 1986-12-04 |
| JPS59120880A (ja) | 1984-07-12 |
| KR840007474A (ko) | 1984-12-07 |
| EP0111449B1 (de) | 1986-10-29 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0101663B1 (de) | Uhr und Verfahren zu ihrer Herstellung | |
| EP0098795A2 (de) | Uhr und Verfahren zur Herstellung derselben | |
| FR2918424A1 (fr) | Ensemble de joint mecanique, notamment ensemble rotulant, ainsi que procede de fabrcation d'un tel ensemble rotulant | |
| EP2738625A1 (de) | Uhrgehäuse umfassend einen Metallfaltenbalg | |
| EP0111449B1 (de) | Verfahren zur Herstellung eines äusseren Uhrenteils und durch dieses Verfahren hergestelltes Teil | |
| FR2510926A1 (fr) | Procede de fabrication de corps de paliers | |
| EP0066538B1 (de) | Uhrgehäuse | |
| EP0197416B1 (de) | Eine aus einem Uhrengehäuseteil und aus einem Armband gebildete Einheit sowie Herstellungsverfahren hierzu | |
| FR2570482A1 (fr) | Tube de chaleur en aluminium, en acier ou fonte grise | |
| FR2595280A1 (fr) | Procede de soudage par diffusion avec pression isostatique | |
| FR2569591A1 (fr) | Plaque refractaire pour obturateurs coulissants de recipients metallurgiques | |
| EP0168010A1 (de) | Uhrengehäuse | |
| WO2021234242A1 (fr) | Procede d'assemblage d'une premiere partie metallique avec une deuxieme partie en materiau composite a matrice organique, et piece resultant d'un tel assemblage | |
| FR2551523A1 (fr) | Plaque d'obturateur pour un obturateur coulissant | |
| EP0097393A1 (de) | Armbanduhrgehäuse | |
| EP4153407A1 (de) | Struktur zur montage eines teils mit einem ersten metallteil und einem zweiten teil aus einem organischen matrixverbundstoff | |
| EP4258065B1 (de) | Verfahren zum zusammenbau eines glases mit einem armbanduhrgehäuse | |
| EP4071557B1 (de) | Gehäuseelement für uhr, das einen drücker aus massivem metallischem glas umfasst | |
| EP0251950A1 (de) | Abdichtungsvorrichtung für die Montage von glatten und parallelen Flächen und entsprechender Dichtung | |
| EP0334182B1 (de) | Uhrengehäuse mit einem Mantel | |
| WO2009125113A2 (fr) | Ensemble de raccordement electrique et procede de fabrication de l'ensemble | |
| EP0842731B1 (de) | Verfahren und Vorrichtung zum Fixieren einer Gelenkstange, mit diesem Verfahren hergestelltes mehrgliedriges Armband | |
| FR2596487A1 (fr) | Procede de realisation d'un composant de robinetterie et composant de robinetterie obtenu par la mise en oeuvre dudit procede | |
| EP0490800A1 (de) | Zylinder für Einzel- oder Doppelrollenstranggiessen. | |
| BE1006550A5 (fr) | Procede de fabrication d'objet en matiere plastique de type composite. |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Designated state(s): CH DE FR GB IT LI |
|
| AK | Designated contracting states |
Designated state(s): CH DE FR GB IT LI |
|
| 17P | Request for examination filed |
Effective date: 19840920 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): CH DE FR GB IT LI |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 19861029 |
|
| REF | Corresponds to: |
Ref document number: 3367288 Country of ref document: DE Date of ref document: 19861204 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20021127 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20021206 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20021209 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20021224 Year of fee payment: 20 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20031204 Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20031204 Ref country code: CH Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20031204 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |