EP0121707A2 - Verfahren zum Schleifen von gestaltlosem Aluminium-Oxyd - Google Patents
Verfahren zum Schleifen von gestaltlosem Aluminium-Oxyd Download PDFInfo
- Publication number
- EP0121707A2 EP0121707A2 EP84101834A EP84101834A EP0121707A2 EP 0121707 A2 EP0121707 A2 EP 0121707A2 EP 84101834 A EP84101834 A EP 84101834A EP 84101834 A EP84101834 A EP 84101834A EP 0121707 A2 EP0121707 A2 EP 0121707A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- aluminum oxide
- polishing
- oxide surface
- citric acid
- silicon dioxide
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- TWNQGVIAIRXVLR-UHFFFAOYSA-N oxo(oxoalumanyloxy)alumane Chemical compound O=[Al]O[Al]=O TWNQGVIAIRXVLR-UHFFFAOYSA-N 0.000 title claims abstract description 44
- 238000005498 polishing Methods 0.000 title claims abstract description 33
- 238000000034 method Methods 0.000 title claims abstract description 28
- VYPSYNLAJGMNEJ-UHFFFAOYSA-N Silicium dioxide Chemical compound O=[Si]=O VYPSYNLAJGMNEJ-UHFFFAOYSA-N 0.000 claims abstract description 36
- KRKNYBCHXYNGOX-UHFFFAOYSA-N citric acid Chemical compound OC(=O)CC(O)(C(O)=O)CC(O)=O KRKNYBCHXYNGOX-UHFFFAOYSA-N 0.000 claims abstract description 30
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims abstract description 12
- 239000003082 abrasive agent Substances 0.000 claims abstract description 4
- 229940075614 colloidal silicon dioxide Drugs 0.000 claims abstract description 3
- 239000000377 silicon dioxide Substances 0.000 claims description 13
- 239000000758 substrate Substances 0.000 claims description 9
- 235000012239 silicon dioxide Nutrition 0.000 claims description 8
- 239000000203 mixture Substances 0.000 claims description 7
- 239000006185 dispersion Substances 0.000 claims description 6
- MTPVUVINMAGMJL-UHFFFAOYSA-N trimethyl(1,1,2,2,2-pentafluoroethyl)silane Chemical compound C[Si](C)(C)C(F)(F)C(F)(F)F MTPVUVINMAGMJL-UHFFFAOYSA-N 0.000 claims description 6
- 239000008367 deionised water Substances 0.000 claims description 4
- 229910021641 deionized water Inorganic materials 0.000 claims description 4
- 238000004544 sputter deposition Methods 0.000 claims description 3
- 239000002344 surface layer Substances 0.000 claims 3
- 239000010410 layer Substances 0.000 claims 1
- 239000002002 slurry Substances 0.000 abstract description 19
- YASYEJJMZJALEJ-UHFFFAOYSA-N Citric acid monohydrate Chemical compound O.OC(=O)CC(O)(C(O)=O)CC(O)=O YASYEJJMZJALEJ-UHFFFAOYSA-N 0.000 abstract description 4
- 239000000463 material Substances 0.000 description 11
- 239000002245 particle Substances 0.000 description 6
- 229910052594 sapphire Inorganic materials 0.000 description 5
- 239000010980 sapphire Substances 0.000 description 5
- XUIMIQQOPSSXEZ-UHFFFAOYSA-N Silicon Chemical compound [Si] XUIMIQQOPSSXEZ-UHFFFAOYSA-N 0.000 description 4
- 238000007517 polishing process Methods 0.000 description 4
- 239000000843 powder Substances 0.000 description 4
- RMAQACBXLXPBSY-UHFFFAOYSA-N silicic acid Chemical compound O[Si](O)(O)O RMAQACBXLXPBSY-UHFFFAOYSA-N 0.000 description 4
- 229910052710 silicon Inorganic materials 0.000 description 4
- 239000010703 silicon Substances 0.000 description 4
- 229910052782 aluminium Inorganic materials 0.000 description 3
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 3
- 238000006243 chemical reaction Methods 0.000 description 3
- 239000008119 colloidal silica Substances 0.000 description 3
- 238000000151 deposition Methods 0.000 description 3
- 239000011148 porous material Substances 0.000 description 3
- 238000001552 radio frequency sputter deposition Methods 0.000 description 3
- 239000000126 substance Substances 0.000 description 3
- 235000012431 wafers Nutrition 0.000 description 3
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 description 2
- VEXZGXHMUGYJMC-UHFFFAOYSA-N Hydrochloric acid Chemical compound Cl VEXZGXHMUGYJMC-UHFFFAOYSA-N 0.000 description 2
- 239000007767 bonding agent Substances 0.000 description 2
- 238000005516 engineering process Methods 0.000 description 2
- 229910002804 graphite Inorganic materials 0.000 description 2
- 239000010439 graphite Substances 0.000 description 2
- 238000003754 machining Methods 0.000 description 2
- 238000005259 measurement Methods 0.000 description 2
- 239000007787 solid Substances 0.000 description 2
- PFNQVRZLDWYSCW-UHFFFAOYSA-N (fluoren-9-ylideneamino) n-naphthalen-1-ylcarbamate Chemical compound C12=CC=CC=C2C2=CC=CC=C2C1=NOC(=O)NC1=CC=CC2=CC=CC=C12 PFNQVRZLDWYSCW-UHFFFAOYSA-N 0.000 description 1
- MARUHZGHZWCEQU-UHFFFAOYSA-N 5-phenyl-2h-tetrazole Chemical compound C1=CC=CC=C1C1=NNN=N1 MARUHZGHZWCEQU-UHFFFAOYSA-N 0.000 description 1
- 239000004593 Epoxy Substances 0.000 description 1
- BQCADISMDOOEFD-UHFFFAOYSA-N Silver Chemical compound [Ag] BQCADISMDOOEFD-UHFFFAOYSA-N 0.000 description 1
- 239000002253 acid Substances 0.000 description 1
- 150000007513 acids Chemical class 0.000 description 1
- 238000007792 addition Methods 0.000 description 1
- 239000000853 adhesive Substances 0.000 description 1
- 230000001070 adhesive effect Effects 0.000 description 1
- PNEYBMLMFCGWSK-UHFFFAOYSA-N aluminium oxide Inorganic materials [O-2].[O-2].[O-2].[Al+3].[Al+3] PNEYBMLMFCGWSK-UHFFFAOYSA-N 0.000 description 1
- VQYHBXLHGKQYOY-UHFFFAOYSA-N aluminum oxygen(2-) titanium(4+) Chemical compound [O-2].[Al+3].[Ti+4] VQYHBXLHGKQYOY-UHFFFAOYSA-N 0.000 description 1
- 238000005229 chemical vapour deposition Methods 0.000 description 1
- 230000015271 coagulation Effects 0.000 description 1
- 238000005345 coagulation Methods 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 230000008021 deposition Effects 0.000 description 1
- UITULIMOLIQGTK-UHFFFAOYSA-N dialuminum 2-hydroxypropane-1,2,3-tricarboxylic acid oxygen(2-) Chemical compound [O-2].[O-2].[O-2].[Al+3].[Al+3].OC(=O)CC(O)(C(O)=O)CC(O)=O UITULIMOLIQGTK-UHFFFAOYSA-N 0.000 description 1
- 239000010432 diamond Substances 0.000 description 1
- 229910003460 diamond Inorganic materials 0.000 description 1
- 238000002050 diffraction method Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000000407 epitaxy Methods 0.000 description 1
- 239000000499 gel Substances 0.000 description 1
- 239000008240 homogeneous mixture Substances 0.000 description 1
- 229910052751 metal Inorganic materials 0.000 description 1
- 239000002184 metal Substances 0.000 description 1
- 238000012544 monitoring process Methods 0.000 description 1
- 238000000465 moulding Methods 0.000 description 1
- 238000001556 precipitation Methods 0.000 description 1
- 238000002360 preparation method Methods 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 230000001681 protective effect Effects 0.000 description 1
- 230000003763 resistance to breakage Effects 0.000 description 1
- 239000004576 sand Substances 0.000 description 1
- 239000004065 semiconductor Substances 0.000 description 1
- 230000035945 sensitivity Effects 0.000 description 1
- 229910052709 silver Inorganic materials 0.000 description 1
- 239000004332 silver Substances 0.000 description 1
- 239000011029 spinel Substances 0.000 description 1
- 229910052596 spinel Inorganic materials 0.000 description 1
- 230000003746 surface roughness Effects 0.000 description 1
- 239000011800 void material Substances 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B37/00—Lapping machines or devices; Accessories
- B24B37/04—Lapping machines or devices; Accessories designed for working plane surfaces
Definitions
- This invention relates to a method of chemical-mechanical polishing of an amorphous aluminum oxide surface.
- Aluminum oxide is a chemically non-reactive, relatively hard material. Polishing of such films which have been deposited upon surfaces of mechanical parts have not been accomplished up to the present.
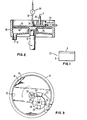
- Fig. 1 illustrates a cross-sectional view of the mechanical part 25 to be polished by the polishing process of the present description.
- the 25 includes a substrate 8 and an amorphous aluminum oxide layer 9 of about 5 to 8 micrometers in thickness formed upon the substrate. It is preferred to utilize as the substrate 8 a combination of aluminum oxide and titanium carbide in a fine grain mixture that has been pressed and sintered or hot pressed. However, titanium carbide particles alone may be compressed into desired parts in a similar fashion.
- the mixture is characterized by an average particle size of less than about 5 microns and preferably the particles are 1 to 2 microns in length.
- the preferred mixture is in the range of about 60 to 80 % aluminum oxide and 40 to 20 % titanium carbide by weight.
- the high density mixture has low porosity and exhibits improvement in Young's and Shear moduli of elasticity and modulus of rupture.
- the materials are ground into powders of the desired particle sizes and mixed in the desired composition of about 80 to 60 % aluminum oxide to 20 to 40 % titanium carbide to a homogeneous mixture.
- the dry powder is measured and poured to fill a graphite pressing mold.
- the powder charge is then precompacted with an applied load of approximately 68.95 to 206.85 bar.
- the precompacted mold is loaded into a hot press and heated to a temperature in the range of 1400°C to 1650°C.
- the pressed part is hot pressed, when the desired temperature is reached at a pressure of between 275.8 and 413.7 bar.
- the pressed part is cooled to room temperature for a desired time to maintain a stress-free condition.
- the cooled part is removed from the mold, deburred and sand blasted to remove any excess graphite.
- the part is now machined to the de - sired shape and dimensions using conventional diamond machining and mechanical lapping methods.
- Amorphous aluminum oxide films can be deposited using chemical vapor deposition or rf sputtering methods.
- the rf sputtering method entails the use of a dielectric target of high purity.
- the target is metallized on one side and bonded to a flat water cooled aluminum disc using a silver epoxy bonding agent or other suitable conducting bonding agents.
- the water cooled aluminum disc forms part of the vacuum chamber wall through a system of vacuum seals and an insulating ring.
- a protective metal shield surrounds the exposed areas of the water cooled aluminum disc at an appropriate spacing of 0.5 cm in order to prevent sputtering from this region.
- the source of power is an rf generator.
- the polishing process for aluminum oxide or the like may be understood with reference to Figs. 2 and 3.
- the polishing machine includes a bowl 10 having a slurry outlet 12 and a driven plate 14. Mounted on the plate 14 by any suitable means (not shown) is a soft, firm surface or pad 16 composed of a poromeric material.
- the pad materials used are true poromeric comprised of a top coat and'substrate layer.
- the thickness of top coat is critical. Top coat thickness is 381-508 ⁇ m, substrate is 508-635 ⁇ m. Total package is 1022 + 50.8 ⁇ m thick.
- the top coat is designed and made by a coagulation process to obtain a macro and micro pore random structure.
- the macro pores are irregularly shaped and randomly dispersed without any preferred orientation in the top coat layer.
- the micro pore comprise the rest of top layer.
- Pads of this type which are commercially available include: Rodel 210 made by Rodel Inc. of Newark, Delaware USA, POLTEX made by the GEOS Corp., Stanford, CT. and NEWMAN polishing pads made by the G. Newman & Co., Santa Clara, California.
- the plate 14 is rotated by means of suitable driving means (not shown) coupled through shaft 18.
- Mechanical parts 25 to be polished are mounted on the plate 20 by means of suitable adhesive or other suitable method.
- This plate 20 with its mounted parts thereon is maintained against the surface 16 by arm 22 having bearing surfaces 26 and a substantial pressure P applied through shaft 28 to urge the wafers strongly against the surface 16.
- the preferred pressure is between about 1.5 x 10 4 to 5.25 ⁇ 10 4 P a (about 150 to 425 gmJcm 2 ).
- the arm 22 is suspended from the polishing bowl edge and positioned on the side of the plate 20 in the path of its normal rotation which is caused by the rotation of plate 14.
- the rotation of plate 14 produces a rotation of the plate 20.
- the surface of the parts 25 is continuously wetted with excess quantity of polishing slurry by flowing it through the pipe 32 with its restricted opening onto the surface 16 of rotating plate 14.
- a parastolic pump 34 moves the slurry through the pipe 32. Excess slurry is splashed from the end of the rotating plate 14 and flows out of the excess slurry opening 12.
- the citric acid-aqueous dispersion of silicon dioxide can be conveniently employed in the form of silica sols and silica gels having silicon dioxide particle sizes in the range of 1 to 500 nm (millimicrons), in concentrations of 6 to 16 weight percent silica.
- Convenient sources of the aqueous dispersion of the silicon dioxide is the trademarked silica sol composition LUDOX colloidal silica made by E.I. Dupont Co., Wilmington, Del., NALCOAG 1034A colloidal silica made by Nalco Chem. Co., Chicago, I11., QUSO silicas made by Philadelphia Quartz Co. of Philadelphia, Pa., SYLOID 701 wafer polishing material made by Davison Chem. Div. of W.R. Grace and Co., Baltimore, Md. and "Syton HT-50" made by Monsanto Company, St. Louis, Mo.,.USA.
- the citric acid-aqueous dispersion of silicon dioxide or silicon dioxide slurry is required to have a pH in the range of about 7 to 9. It is preferable that the slurry have a pH slightly basic and of the order of 8.
- the basic pH may be obtained by adding small quantities of citric acid solution of 80 grams/liter water to the dilute silicon dioxide slurry to produce the desired pH.
- the slurry with the citric acid is stable for 48 hours without any gelling or precipitation. Slurries with other acids such as hydrochloric acid are stable for only short periods of time. At higher pH than 9 the surface will roughen, giving an orange-peel like effect. Lower pH polishing produces undesirably slow polishing rates.
- the polishing time is also dependent upon the pre-polishing surface roughness condition.
- the roughness of the pre-polishing surface is about 101.6 nm (peak to valley height).
- the roughness of the pre-polishing surface depends upon the roughness of the substrate upon which the alumina is deposited, and upon the deposition method. That is the reason there is needed a highly perfect, polished substrate. The film is too thin for lapping, that is it cannot be abrasively polished for the same reason plus damage.
- a chemical mechanical polishing process for polishing aluminum oxide operates very effectively to produce surface finishes of less than the order of 5.08 nm (0.2 micro inches) (peak to valley height). This measurement is actually the lower limit of the equipment so the surface finish is even better than that 5.08 nm.
- the surface finish is measured by the conventional stylus method.
- citric acid water slurry has a reaction between the aluminum oxide and the water in the slurry to form an aluminum oxide-citric acid complex on the specimen surface which is in turn removed by the silicon dioxide slurry and polishing pad.
- the apparent chemical reaction is: citric acid complex i
- the resulting polishing produces under these conditions no relief between the aluminum oxide grain boundaries and a highly perfect surface.
- An amorphous aluminum oxide layer having a thickness of 5-8 ⁇ m was formed onto aluminum oxide-titanium carbide mechanical parts made by the high temperature pressure molding technique described above in the specification.
- the aluminum oxide layer was formed thereon by the sputtering process as described above. These parts were placed in the polishing apparatus illustrated by Fig. 2 and 3.
- a mixtue of 1 part silica sol with 4 parts of deionized water was prepared.
- the silica sol has a silica content of about 50 weight percent with maximum partical size of 40 to 45 nm. This slurry has a solids content of 10 weight percent silica.
- a citric acid solution comprising 80 grams citric acid in one liter of deionized water was added to the silica sol slurry while monitoring the pH of the solution. The solution was adjusted to a pH of 8 in this manner.
- the polishing pressure used was 2.225 x 10 4 Pa.
- the removal rate was 1.5 ⁇ m/hour.
- the polished surface is rinsed in deionized water.
- the polished surface finish (peak to valley) was 5.08 nm as determined by the conventional stylus method described in "Report on the Measurement of Surface Finish by Stylus Methods" by R.E. Reason, et al., published by the Rank Taylor Hobson Division Leicester, England 1944.
- the resulting surfaces were flat to less than 1 ⁇ m over the part surface and void of polishing induced defects.
- Amorphous aluminum oxide layers were prepared as in the Example 1. They were polished as described in Example 1 using pH of 9.5 and 11. the surfaces were visually unacceptable, due to pits and orange-peel. No removal rate data taken.
- the pH was adjusted with citric acid additions. At pH of 6 polishing was very slow and impossible to measure accurately. At pH of 7 to 9 as best as could be determined the removal rate was 2-3 ⁇ m per hour at a pressure of 3.75 x 10 4 Pa.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Finish Polishing, Edge Sharpening, And Grinding By Specific Grinding Devices (AREA)
- Compounds Of Alkaline-Earth Elements, Aluminum Or Rare-Earth Metals (AREA)
- Mechanical Treatment Of Semiconductor (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US47412083A | 1983-03-10 | 1983-03-10 | |
| US474120 | 1983-03-10 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0121707A2 true EP0121707A2 (de) | 1984-10-17 |
| EP0121707A3 EP0121707A3 (en) | 1985-10-09 |
| EP0121707B1 EP0121707B1 (de) | 1988-09-07 |
Family
ID=23882264
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19840101834 Expired EP0121707B1 (de) | 1983-03-10 | 1984-02-22 | Verfahren zum Schleifen von gestaltlosem Aluminium-Oxyd |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0121707B1 (de) |
| JP (1) | JPS5953317B2 (de) |
| DE (1) | DE3473846D1 (de) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0593057A1 (de) * | 1992-10-15 | 1994-04-20 | Applied Materials, Inc. | Flachläppvorrichtung und Verfahren zur Durchführung eines Flachläppprozesses |
| EP1298336A3 (de) * | 2001-09-27 | 2005-04-20 | Nsk Ltd | Nadellager und Verfahren zum Schleifen von Lagerteilen dieses Lagers |
Families Citing this family (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5643053A (en) * | 1993-12-27 | 1997-07-01 | Applied Materials, Inc. | Chemical mechanical polishing apparatus with improved polishing control |
| US5582534A (en) * | 1993-12-27 | 1996-12-10 | Applied Materials, Inc. | Orbital chemical mechanical polishing apparatus and method |
| US5650039A (en) * | 1994-03-02 | 1997-07-22 | Applied Materials, Inc. | Chemical mechanical polishing apparatus with improved slurry distribution |
| US5527423A (en) * | 1994-10-06 | 1996-06-18 | Cabot Corporation | Chemical mechanical polishing slurry for metal layers |
| US5858813A (en) * | 1996-05-10 | 1999-01-12 | Cabot Corporation | Chemical mechanical polishing slurry for metal layers and films |
| TW572980B (en) | 2000-01-12 | 2004-01-21 | Jsr Corp | Aqueous dispersion for chemical mechanical polishing and chemical mechanical polishing process |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| BE549314A (de) * | 1955-07-08 | |||
| CH356000A (de) * | 1955-07-08 | 1961-07-31 | Vaw Ver Aluminium Werke Ag | Verfahren zur Herstellung haltbarer hochglänzender Oberflächen auf Werkstücken aus Aluminium oder einer Aluminiumlegierung |
| DE1009884B (de) * | 1955-07-08 | 1957-06-06 | Vaw Ver Aluminium Werke Ag | Verfahren zur Vorbehandlung von Werkstuecken aus Aluminium oder Aluminiumlegierungen zur Herstellung hochglaenzender, anodisch oxydierter Oberflaechen |
| US2940228A (en) * | 1956-07-03 | 1960-06-14 | Vaw Ver Aluminium Werke Ag | Apparatus for polishing metals |
| US2942956A (en) * | 1958-10-13 | 1960-06-28 | Wyandotte Chemicals Corp | Aluminum brightener compositions |
| US3053646A (en) * | 1960-07-15 | 1962-09-11 | Dow Chemical Co | Grinding and polishing compositions and method of making same |
| DE1271288B (de) * | 1965-02-23 | 1968-06-27 | Monsanto Co | Verfahren zum Polieren von Werkstoffen mittels eines Siliciumdioxyd enthaltenden Poliermittels |
| GB1109892A (en) * | 1965-03-12 | 1968-04-18 | Marshall Wolverhampton | A new or improved metal polishing composition |
| US3906678A (en) * | 1972-09-14 | 1975-09-23 | Buehler Ltd | Automatic specimen polishing machine and method |
| US3931696A (en) * | 1974-03-04 | 1976-01-13 | Veb Rathenower Optische Werke | Device for making sections for specimens and specimen supports therefor |
-
1983
- 1983-11-30 JP JP58224563A patent/JPS5953317B2/ja not_active Expired
-
1984
- 1984-02-22 DE DE8484101834T patent/DE3473846D1/de not_active Expired
- 1984-02-22 EP EP19840101834 patent/EP0121707B1/de not_active Expired
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0593057A1 (de) * | 1992-10-15 | 1994-04-20 | Applied Materials, Inc. | Flachläppvorrichtung und Verfahren zur Durchführung eines Flachläppprozesses |
| EP1298336A3 (de) * | 2001-09-27 | 2005-04-20 | Nsk Ltd | Nadellager und Verfahren zum Schleifen von Lagerteilen dieses Lagers |
| US6910948B2 (en) | 2001-09-27 | 2005-06-28 | Nsk Ltd. | Needle bearing and method for grinding bearing parts thereof |
Also Published As
| Publication number | Publication date |
|---|---|
| JPS59170175A (ja) | 1984-09-26 |
| EP0121707A3 (en) | 1985-10-09 |
| DE3473846D1 (en) | 1988-10-13 |
| JPS5953317B2 (ja) | 1984-12-24 |
| EP0121707B1 (de) | 1988-09-07 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0121706B1 (de) | Verfahren zum Schleifen von Titan-Karbid enthaltenden Flächen | |
| US6293854B1 (en) | Dresser for polishing cloth and manufacturing method therefor | |
| EP1446263B1 (de) | Verfahren zum polieren der oberfläche eines substrats | |
| JP5455282B2 (ja) | シリコン・オン・インシュレータ搬送ウエハのエッジ除去 | |
| US6406923B1 (en) | Process for reclaiming wafer substrates | |
| US4244775A (en) | Process for the chemical etch polishing of semiconductors | |
| JP2011238952A (ja) | Cmp生成物 | |
| EP2930751B1 (de) | Griffsubstrat für ein verbundsubstrat zur verwendung mit einem halbleiter | |
| WO2008078666A1 (en) | Water-based polishing slurry for polishing silicon carbide single crystal substrate, and polishing method for the same | |
| CN101547770A (zh) | Cmp修整器和其制备方法 | |
| JP2004096112A (ja) | 半導体ウェーハの処理法 | |
| JP2006222453A (ja) | シリコンウエーハの製造方法及びシリコンウエーハ並びにsoiウエーハ | |
| EP0121707B1 (de) | Verfahren zum Schleifen von gestaltlosem Aluminium-Oxyd | |
| KR930004114B1 (ko) | 반도체기판 연마용 연마액과 연마방법 | |
| EP2871668B1 (de) | Griffsubstrat für ein verbundsubstrat zur verwendung mit einem halbleiter | |
| CA2169392A1 (en) | Method and apparatus for polishing metal-soluble materials such as diamond | |
| JPH11170155A (ja) | 研磨装置 | |
| US4108716A (en) | Polishing of CdS crystals | |
| EP1201367A1 (de) | Vorrichtung zum Abrichten eines Polierkissens und Verfahren zum Herstellen des Polierkissens | |
| CN117736653A (zh) | 一种用于单晶硅化学机械抛光的抛光液及化学机械抛光方法 | |
| JP4464019B2 (ja) | 研磨用ワーク保持盤及びワークの研磨装置及び研磨方法 | |
| WO1998044541A1 (en) | Flattening process for semiconductor wafers | |
| CN1227404A (zh) | 半导体装置的制造方法 | |
| CN101176983A (zh) | 铜片衬底的半固着磨粒抛光方法 | |
| JP3482313B2 (ja) | 半導体基板用研磨布のドレッサーおよびその製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): DE FR GB |
|
| 17P | Request for examination filed |
Effective date: 19841123 |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Designated state(s): DE FR GB |
|
| 17Q | First examination report despatched |
Effective date: 19860708 |
|
| D17Q | First examination report despatched (deleted) | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB |
|
| REF | Corresponds to: |
Ref document number: 3473846 Country of ref document: DE Date of ref document: 19881013 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19920124 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19920304 Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19931029 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19931103 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19940118 Year of fee payment: 11 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19950222 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19950222 |