EP0143335A1 - Dispositif pour la fabrication de filaments ondulés à partir de tabac reconstitué - Google Patents
Dispositif pour la fabrication de filaments ondulés à partir de tabac reconstitué Download PDFInfo
- Publication number
- EP0143335A1 EP0143335A1 EP84112877A EP84112877A EP0143335A1 EP 0143335 A1 EP0143335 A1 EP 0143335A1 EP 84112877 A EP84112877 A EP 84112877A EP 84112877 A EP84112877 A EP 84112877A EP 0143335 A1 EP0143335 A1 EP 0143335A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- nozzle head
- tobacco
- insert
- thread
- intermediate products
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 241000208125 Nicotiana Species 0.000 title claims abstract description 42
- 235000002637 Nicotiana tabacum Nutrition 0.000 title claims abstract description 42
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 8
- 239000000835 fiber Substances 0.000 claims abstract description 30
- 239000013067 intermediate product Substances 0.000 claims abstract description 18
- 238000002788 crimping Methods 0.000 claims abstract description 6
- 239000000428 dust Substances 0.000 claims abstract description 6
- 239000000654 additive Substances 0.000 claims abstract description 5
- 239000011230 binding agent Substances 0.000 claims abstract description 5
- 239000002699 waste material Substances 0.000 claims abstract description 5
- 239000000203 mixture Substances 0.000 claims abstract 5
- 238000000034 method Methods 0.000 claims description 8
- 230000008569 process Effects 0.000 claims description 3
- 238000000926 separation method Methods 0.000 claims description 3
- 239000012530 fluid Substances 0.000 claims description 2
- 238000012545 processing Methods 0.000 claims description 2
- 239000000543 intermediate Substances 0.000 claims 1
- 230000007704 transition Effects 0.000 description 4
- 239000002245 particle Substances 0.000 description 3
- 239000004033 plastic Substances 0.000 description 3
- 238000002360 preparation method Methods 0.000 description 3
- 244000061176 Nicotiana tabacum Species 0.000 description 2
- 235000019504 cigarettes Nutrition 0.000 description 2
- 238000001816 cooling Methods 0.000 description 2
- 230000000875 corresponding effect Effects 0.000 description 2
- 238000005520 cutting process Methods 0.000 description 2
- 238000012958 reprocessing Methods 0.000 description 2
- 239000000126 substance Substances 0.000 description 2
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 2
- 239000000853 adhesive Substances 0.000 description 1
- 230000001070 adhesive effect Effects 0.000 description 1
- 230000006399 behavior Effects 0.000 description 1
- 238000004140 cleaning Methods 0.000 description 1
- 238000001035 drying Methods 0.000 description 1
- 230000002349 favourable effect Effects 0.000 description 1
- 239000000945 filler Substances 0.000 description 1
- 239000011888 foil Substances 0.000 description 1
- 239000008187 granular material Substances 0.000 description 1
- 238000011086 high cleaning Methods 0.000 description 1
- 230000006872 improvement Effects 0.000 description 1
- 230000001788 irregular Effects 0.000 description 1
- 239000007788 liquid Substances 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 238000002156 mixing Methods 0.000 description 1
- 230000000704 physical effect Effects 0.000 description 1
- 235000021395 porridge Nutrition 0.000 description 1
- 238000012805 post-processing Methods 0.000 description 1
- 239000000047 product Substances 0.000 description 1
- 239000002994 raw material Substances 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- 238000007493 shaping process Methods 0.000 description 1
- 230000000391 smoking effect Effects 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B11/00—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses
- B30B11/22—Extrusion presses; Dies therefor
- B30B11/221—Extrusion presses; Dies therefor extrusion dies
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24B—MANUFACTURE OR PREPARATION OF TOBACCO FOR SMOKING OR CHEWING; TOBACCO; SNUFF
- A24B3/00—Preparing tobacco in the factory
- A24B3/14—Forming reconstituted tobacco products, e.g. wrapper materials, sheets, imitation leaves, rods, cakes; Forms of such products
Definitions
- the invention relates to a method and an apparatus for producing crimped fiber pieces from reprocessed tobacco of the type specified.
- EP-OS 0039647 shows a device in which the device is opened again prepared tobacco mass is compressed by the screw of an extruder in a narrowing outlet area and is then pressed through a nozzle plate in front of which a cutting knife is arranged.
- the disadvantage here is the relatively high cleaning effort, since the entire device must be taken apart for thorough cleaning of this extruder.
- a method and a device of the specified type are apparent from DE-PS 1 432 567, the thread-like intermediate products having to be subjected to a subsequent, very complex post-processing in order to obtain the desired, crimped fiber pieces.
- the thread-like intermediate products which have a circular cross-section, have to be rolled into intermediate products with a flat cross-section and then dried in an air dryer, which ultimately results in the crimped fiber pieces.
- the invention is therefore based on the object of providing a method and a device for producing crimped fiber pieces from recycled tobacco of the type specified, in which the disadvantages mentioned above do not occur.
- the advantages achieved with the invention are especially based on the fact that once the desired crimped fiber pieces result in cutting of the nozzle head leaving, filamentary intermediate products, their dimensions and their behavior, in particular in the cigarette manufacturing, so the corresponding properties of the S chnittabaks tuned that, for example, they can be immediately fed into the manufacture of cigarettes, that is, they do not have to go through tobacco preparation.
- the streamlined design of the nozzle head which is achieved by the process step of shaping the plastic, strand-like tobacco mass into a thin-walled tube, results in a substantial reduction in the risk of clogging, that is to say that such an extruder can be operated with relatively long maintenance intervals because of a fault only rarely occurs.
- the thin-walled tube is only cut into individual threads immediately before leaving the device according to the invention, which results in thread-like, crimped intermediate products due to the guidance of the plastic mass and the angle of the insert, which only need to be separated into the individual, crimped fiber pieces, before the ripple through with her Length increasing weight of the thread-like intermediate products is reduced or canceled.
- the thin outlet grooves and the entire nozzle head can be easily cleaned, since only the insert has to be removed and then all surfaces to be cleaned are easily accessible.
- a possible blockage of the thin outlet grooves can also be quickly removed during operation, since only the insert has to be rotated slightly; the resulting shear forces loosen the adhesive masses so that they are carried away by the emerging mass.
- a simple round-strand die head of a conventional laboratory extruder can also be converted to produce the crimped fiber pieces, in that such an insert is fastened, for example screwed, directly into the mouth of the die head.
- the outlet grooves should be designed in such a way that the cross section of the exiting, thread-like intermediate products deviates as much as possible from the circular cross section, since the internal stresses of the product during the cooling from the plastic to the solid state mean that very strong twisting or crimping of the tobacco threads can be achieved.
- a particularly good crimp of the fiber pieces results if they have a flat, rectangular to slightly lenticular cross-section when they emerge from the nozzle head and pieces that are approx. 10 to 20 mm long are cut by a rotating knife immediately after they exit before the crimping by the the weight of the crimped fiber pieces, which increases with the fiber length, is smoothed (pulled).
- a further improvement in the crimping of the fiber pieces can be achieved by designing the rotating knives or the receiving device for the rotating knives in a propeller-like manner. Due to the turbulent air turbulence and the mechanical stress on impact with the propeller-shaped knives, the still formable fiber sections are given an even more irregular, spatial contour. This process works very economically, since the individual components are mixed in the dry state and then the mass can be brought to only about 16% moisture by adding liquid, in particular water. In contrast to other processes, no porridge, dough or granules are required.
- the finished, crimped fiber pieces have a humidity of about 10 to 12% after cooling from the temperature between 130 and 160 ° C, as is usually the case in the nozzle head, to the ambient temperature, so that no additional drying process is necessary.
- the crimped fiber pieces should have a thickness of 0.1 to 0.3 mm, in particular 0.15 to 0.25 mm, a width of 0.4 to 3 mm, in particular 0.6 to 1.5 mm, and a ge stretched length of 5 to 40 mm, in particular 8 to 20 mm; They can be made from tobacco particles with a maximum particle size of 0.5 mm (ie tobacco particles that pass through a sieve with a mesh size of 0.5 mm) with the addition of binders and the additives customary in tobacco processing and without further treatment the cut or smoking tobacco are added,
- the device shown in FIG. 1, generally indicated by the reference numeral 10, for producing crimped fiber pieces from recycled tobacco has a mixer 12 with a housing 14 and a rotating mixing tool 16, which is rotated via a drive motor 18.
- the mixer 12 is supplied with the components required for the reprocessing of tobacco dust and / or tobacco waste, namely the tobacco dust, binder, water and the additives customary in the tobacco industry, for example flavorings, fillers, fire-influencing substances, color-influencing substances etc.
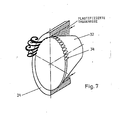
- the mixed, pulverulent raw material discharged from the mixer 12 passes via a hopper 22 into an extruder 20, at the nozzle head 24 of which thread-like intermediate products emerge. These thread-like intermediate products of the nozzle head 24 are cut into the crimped tobacco threads by a rotating knife 26, which is rotated by a drive motor 28.
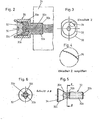
- the die head 24 of the extruder 20 has a stepped, cylindrical outlet sleeve 30, which consists of a cylindrical inlet region 30a and a subsequent cylindrical outlet region 30b, which has a larger inner diameter than the inlet region 30a.
- An insert 32 which can be seen in particular in FIG. 5, is arranged in the outlet sleeve 30 of the nozzle head 24.
- This insert 32 has a cylindrical inlet region 32a, the outside diameter of which is somewhat smaller than the inside of the inlet area 30a of the outlet sleeve 30, an adjoining, approximately cylindrical transition area 32b and a frustoconically widening end area 32c, the end face of which is flush with the end face of the outlet sleeve 30.
- the cylindrical inlet region 32a of the insert 32 is hollow, that is to say it has a cylindrical, continuous bore 32d, as can be seen in FIGS. 2 and 5.
- the transition area 32b and the beginning of the frustoconical end area 32c are provided with four axially extending slots 32e (see also FIG. 6) which connect the bore 32d to the outer surface of this area of the insert 32.
- the end region of the end region 32c again lying on a cylindrical surface in the illustrated embodiment, is provided with flat, rectangular to slightly lenticular outlet grooves 34 (see also FIGS. 3 and 4).
- the insert 32 is screwed into the outlet sleeve 30 by means of the hexagon 36, which in turn is then screwed into the mouth of the nozzle head 24 of a suitable extruder.
- the plasticized, tubular mass has a movement component running perpendicular to the cylinder axis, so that continuous, crimped threads emerge from the lenticular exit grooves 34, which split the thin-walled tube into individual threads, as can be seen in FIGS. 2 and 7.
- the reprocessed tobacco mass therefore leaves the nozzle head 24 or, in a laboratory extruder, the outlet sleeve 30 as a thread-like, crimped intermediate product which is cut by the rotating, propeller-like knife 26 into the crimped, short fiber pieces before the crimping increases with the length of the threads Dead weight is reduced again or canceled entirely.
- the filamentary intermediate products can also be divided into the crimped fiber pieces by a sharp jet from a fluid medium, for example an air jet.
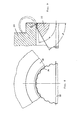
- the frustoconical end region 32c extends approximately at an angle of ⁇ 60 ° to the end face of the insert 32 and then merges into the exit grooves 34, which form an angle of ⁇ 80 ° with the end face of the insert.
- the condition ⁇ ⁇ ⁇ ⁇ ⁇ 90 ° must be fulfilled.
- exit edge between the exit grooves 34 on the one hand and the end face of the insert 32 on the other hand should be designed as a flow separation edge and therefore as sharp as possible.
- the exit edge of the cylindrical outer sleeve 30 or the nozzle head 24 opposite this sharp-edged tear-off edge is rounded and has a radius of 0.3 mm to 5 mm, in particular 0.5 mm to 2 mm; a radius of 0.7 mm is indicated in FIG.
- the end face of the outer sleeve 30 or the nozzle head 24 should be designed such that the dash dot indicated "tobacco thread” can ripple outwards without interference. In the embodiment according to FIG. 9, this is achieved by turning the end face.
- the plasticized tobacco mass enters the gap between the conical insert 32 and the outer sleeve 30 or the nozzle head 24 on the other hand at a relatively low speed and becomes faster when the lenticular exit grooves 34 are reached accelerates.
- the sharp-edged flow separation edge on the insert 32 and the rounded edge on the nozzle head 24 or on the outer sleeve 30 cause the emerging tobacco thread to lie against the rounded edge and thereby be deflected outwards; this results in a strong, unimpeded crimp, which leads to the desired shapes of the fiber pieces.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacture Of Tobacco Products (AREA)
- Extrusion Moulding Of Plastics Or The Like (AREA)
- Manufacturing Of Cigar And Cigarette Tobacco (AREA)
- Nonwoven Fabrics (AREA)
- Cigarettes, Filters, And Manufacturing Of Filters (AREA)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT84112877T ATE28259T1 (de) | 1983-10-28 | 1984-10-25 | Vorrichtung zur herstellung von gekraeuselten faserstuecken aus wiederaufbereitetem tabak. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3339247 | 1983-10-28 | ||
| DE3339247A DE3339247C1 (de) | 1983-10-28 | 1983-10-28 | Verfahren und Vorrichtung zur Herstellung von gekraeuselten Faserstuecken aus wiederaufbereitetem Tabak |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0143335A1 true EP0143335A1 (fr) | 1985-06-05 |
| EP0143335B1 EP0143335B1 (fr) | 1987-07-15 |
Family
ID=6213018
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP84112877A Expired EP0143335B1 (fr) | 1983-10-28 | 1984-10-25 | Dispositif pour la fabrication de filaments ondulés à partir de tabac reconstitué |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US4598721A (fr) |
| EP (1) | EP0143335B1 (fr) |
| AT (1) | ATE28259T1 (fr) |
| DE (2) | DE3339247C1 (fr) |
| ES (1) | ES8506430A1 (fr) |
Cited By (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0232176A3 (fr) * | 1986-02-05 | 1989-01-25 | R.J. Reynolds Tobacco Company | Procédé pour fabriquer de la matière en tabac reconstitué |
| EP0256824A3 (fr) * | 1986-08-11 | 1989-01-25 | R.J. Reynolds Tobacco Company | Traitement des feuilles de tabac |
| EP0238298A3 (fr) * | 1986-03-17 | 1989-01-25 | R.J. Reynolds Tobacco Company | Procédé pour fabriquer de la matière en tabac reconstitué |
| EP0428978A1 (fr) * | 1989-11-21 | 1991-05-29 | Bühler Ag | Dispositif d'extrusion |
| EP0443321A3 (en) * | 1990-02-22 | 1991-11-21 | B.A.T. Cigarettenfabriken Gmbh | Tobacco sheet and process and apparatus for its preparation |
| EP0345477A3 (fr) * | 1988-06-08 | 1992-06-03 | British-American Tobacco (Germany) GmbH | Procédé et dispositif de fabrication de pièces de feuilles de tabac à partir de tabac reconstitué |
| EP0524379A3 (en) * | 1991-05-27 | 1993-03-17 | B.A.T. Cigarettenfabriken Gmbh | Tobacco containing filaments and method and apparatus for their preparation |
| CN112971198A (zh) * | 2019-12-02 | 2021-06-18 | 秦皇岛烟草机械有限责任公司 | 一种新型滚刀式烟草切丝机刀辊体 |
Families Citing this family (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4880018A (en) * | 1986-02-05 | 1989-11-14 | R. J. Reynolds Tobacco Company | Extruded tobacco materials |
| US4768527A (en) * | 1987-01-23 | 1988-09-06 | R. J. Reynolds Tobacco Company | Tobacco material processing |
| US4821749A (en) * | 1988-01-22 | 1989-04-18 | R. J. Reynolds Tobacco Company | Extruded tobacco materials |
| US5129409A (en) * | 1989-06-29 | 1992-07-14 | R. J. Reynolds Tobacco Company | Extruded cigarette |
| CA2466075C (fr) * | 1992-03-25 | 2007-05-01 | Japan Tobacco, Inc. | Matiere entrant dans la composition d'une cigarette; la cigarette ainsi constituee |
| DE4218666C1 (de) * | 1992-06-05 | 1993-12-16 | Bat Cigarettenfab Gmbh | Verfahren und Vorrichtung zur Strukturierung von Tabakmaterialien |
| US5709229A (en) * | 1995-01-28 | 1998-01-20 | Friedrich Priehs | Method of producing a tobacco product for smoking |
| DE10007485A1 (de) * | 2000-02-18 | 2001-08-23 | Hauni Maschinenbau Ag | Verfahren und Vorrichtung zur Verwertung von Tabakstaub |
| GB0011351D0 (en) * | 2000-05-12 | 2000-06-28 | British American Tobacco Co | Tobacco reconstitution |
| DE10065132A1 (de) * | 2000-12-29 | 2002-07-04 | Hauni Maschinenbau Ag | Verfahren zur Herstellung von Agglomeraten und entsprechendes Agglomerat |
| RS54739B1 (sr) | 2011-05-31 | 2016-10-31 | Philip Morris Products Sa | Štapići za upotrebu u proizvodima za pušenje |
| ITRM20130684A1 (it) * | 2013-12-12 | 2015-06-13 | Stefano Bolla | Contenitore ecocompatibile per riciclaggio mozziconi di sigaretta. |
| US20200035118A1 (en) | 2018-07-27 | 2020-01-30 | Joseph Pandolfino | Methods and products to facilitate smokers switching to a tobacco heating product or e-cigarettes |
| US10897925B2 (en) | 2018-07-27 | 2021-01-26 | Joseph Pandolfino | Articles and formulations for smoking products and vaporizers |
| KR102389825B1 (ko) * | 2018-10-17 | 2022-04-25 | 주식회사 케이티앤지 | 에어로졸 생성 물품 |
| CN110301676A (zh) * | 2019-06-27 | 2019-10-08 | 广东中烟工业有限责任公司 | 一种防止烟丝掉落的加热不燃烧烟草基体及其应用 |
| WO2021144043A1 (fr) * | 2020-01-16 | 2021-07-22 | Garbuio S.P.A. | Procédé de production d'une pâte de tabac et de tabac reconstitué, film contenant du tabac et système de production de tabac reconstitué |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH429539A (fr) * | 1964-05-07 | 1967-01-31 | British American Tobacco Co | Filière pour extruder une matière à l'état plastique |
| US3313003A (en) * | 1963-10-04 | 1967-04-11 | Brown & Williamson Tobacco Corp | Extrusion dies for plastic materials |
| DE1529846A1 (de) * | 1961-07-11 | 1970-01-02 | Deutsche Grammophon Gmbh | Presskopf fuer Doppelschneckenextruder |
| US3932081A (en) * | 1972-12-22 | 1976-01-13 | Tamag/Basel Ag | Extruder nozzle for shaping a pulp to form smokable strands or fibers |
| EP0039647A1 (fr) * | 1980-05-06 | 1981-11-11 | Clextral | Dispositif de fabrication de filaments de tabac |
Family Cites Families (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3209763A (en) * | 1961-04-05 | 1965-10-05 | Lorillard Co P | Method for making tobacco products |
| GB983928A (en) * | 1962-05-03 | 1965-02-24 | British American Tobacco Co | Improvements relating to the production of tobacco smoking materials |
| LU74233A1 (fr) * | 1976-01-23 | 1977-07-27 |
-
1983
- 1983-10-28 DE DE3339247A patent/DE3339247C1/de not_active Expired
-
1984
- 1984-10-25 EP EP84112877A patent/EP0143335B1/fr not_active Expired
- 1984-10-25 AT AT84112877T patent/ATE28259T1/de not_active IP Right Cessation
- 1984-10-25 DE DE8484112877T patent/DE3464687D1/de not_active Expired
- 1984-10-26 ES ES537079A patent/ES8506430A1/es not_active Expired
- 1984-10-29 US US06/665,838 patent/US4598721A/en not_active Expired - Fee Related
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1529846A1 (de) * | 1961-07-11 | 1970-01-02 | Deutsche Grammophon Gmbh | Presskopf fuer Doppelschneckenextruder |
| US3313003A (en) * | 1963-10-04 | 1967-04-11 | Brown & Williamson Tobacco Corp | Extrusion dies for plastic materials |
| CH429539A (fr) * | 1964-05-07 | 1967-01-31 | British American Tobacco Co | Filière pour extruder une matière à l'état plastique |
| US3932081A (en) * | 1972-12-22 | 1976-01-13 | Tamag/Basel Ag | Extruder nozzle for shaping a pulp to form smokable strands or fibers |
| EP0039647A1 (fr) * | 1980-05-06 | 1981-11-11 | Clextral | Dispositif de fabrication de filaments de tabac |
Cited By (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0232176A3 (fr) * | 1986-02-05 | 1989-01-25 | R.J. Reynolds Tobacco Company | Procédé pour fabriquer de la matière en tabac reconstitué |
| EP0238298A3 (fr) * | 1986-03-17 | 1989-01-25 | R.J. Reynolds Tobacco Company | Procédé pour fabriquer de la matière en tabac reconstitué |
| EP0256824A3 (fr) * | 1986-08-11 | 1989-01-25 | R.J. Reynolds Tobacco Company | Traitement des feuilles de tabac |
| EP0345477A3 (fr) * | 1988-06-08 | 1992-06-03 | British-American Tobacco (Germany) GmbH | Procédé et dispositif de fabrication de pièces de feuilles de tabac à partir de tabac reconstitué |
| EP0428978A1 (fr) * | 1989-11-21 | 1991-05-29 | Bühler Ag | Dispositif d'extrusion |
| EP0443321A3 (en) * | 1990-02-22 | 1991-11-21 | B.A.T. Cigarettenfabriken Gmbh | Tobacco sheet and process and apparatus for its preparation |
| EP0524379A3 (en) * | 1991-05-27 | 1993-03-17 | B.A.T. Cigarettenfabriken Gmbh | Tobacco containing filaments and method and apparatus for their preparation |
| CN112971198A (zh) * | 2019-12-02 | 2021-06-18 | 秦皇岛烟草机械有限责任公司 | 一种新型滚刀式烟草切丝机刀辊体 |
Also Published As
| Publication number | Publication date |
|---|---|
| ES537079A0 (es) | 1985-08-01 |
| DE3464687D1 (en) | 1987-08-20 |
| ATE28259T1 (de) | 1987-08-15 |
| DE3339247C1 (de) | 1985-05-09 |
| ES8506430A1 (es) | 1985-08-01 |
| EP0143335B1 (fr) | 1987-07-15 |
| US4598721A (en) | 1986-07-08 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0143335B1 (fr) | Dispositif pour la fabrication de filaments ondulés à partir de tabac reconstitué | |
| DE2426492C2 (de) | Verfahren und Vorrichtung zum kontinuierlichen Herstellen von gestreiften Seifenstücken | |
| DE1657244B1 (de) | Verfahren und Vorrichtung zur Herstellung von Faserstaebchen,insbesondere zur Verwendung als Zigarettenfilter | |
| DE202004019711U1 (de) | Vorrichtung zur Herstellung von zerkleinertem Tabakmaterial | |
| DE2121914A1 (de) | Vorrichtung und Verfahren zum Strangpressen von thermoplastischen Kunststoffen | |
| DE1132896B (de) | Verfahren zur Herstellung von koernigen oder zylinderfoermigen Granulaten | |
| CH275420A (de) | Verfahren zur Herstellung von Tabakprodukten wie Stumpen und Cigarillos, und Vorrichtung zur Durchführung des Verfahrens. | |
| DE3343788A1 (de) | Verfahren und vorrichtung zur trennung von produkten oder werkstoffmischungen aus faserigen werkstoffen und nichtfaserigen werkstoffen | |
| EP0617050A1 (fr) | Procédé et dispositif pour l'obtention d'un produit à base d'amidon non modifié, de préference une mousse | |
| EP0113402B1 (fr) | Procédé et dispositif pour la fabrication d'un propergol mono- ou multi-base | |
| CH434700A (de) | Granuliervorrichtung, insbesondere für thermoplastische Kunststoffe und Verfahren zu ihrem Betrieb | |
| EP1827142A1 (fr) | Defibrage de matieres premieres du tabac | |
| EP0629722B1 (fr) | Bande fibreuse comprenant des rubans multiples et procédé et dispositif pour la production | |
| DE1931137C3 (de) | Wiederhergestelltes Zigarettenfilter und Verfahren zu seiner Herstellung | |
| DE1632236B2 (de) | Tabakfilter und verfahren zu seiner herstellung | |
| DE1517290A1 (de) | Verfahren zur Nutzbarmachung und Veredelung von Tabakstaub und anderem Tabakabfall | |
| EP1219186A2 (fr) | Procédé de préparation d'agglomérats et agglomérat correspondant | |
| DE102007040536A1 (de) | Formgebungswerkzeug | |
| DE2841652A1 (de) | Verfahren und vorrichtung zum einspritzen von fluessigkeiten in eine reinigungsmittelmasse | |
| DE3500067A1 (de) | Verfahren und vorrichtung zur herstellung verbrennbarer huelsen auf nitrozellulose-basis als munitionsformteil fuer rohrwaffen | |
| DE3044577C2 (de) | Verfahren und Vorrichtung zur kontinuierlichen Herstellung von Treibladungspulver | |
| DE69212748T2 (de) | Apparat zum Rekuperieren heterogener Abfälle, insbesonderen heterogener Kunststoff-Abfälle | |
| EP0524379B1 (fr) | Filaments contenant du tabac ainsi que leurs procédé et appareil pour les fabriquer | |
| DE3130968A1 (de) | Verfahren und vorrichtung zur kontinuierlichen herstellung von beluefteten zuckermassen | |
| DE2626067C2 (de) | Verfahren zum Texturieren einer als Myzelium vorliegenden, als Nahrungsmittel dienenden Pilzmasse und Vorrichtung zur Durchführung des Verfahrens |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): AT CH DE FR GB IT LI NL |
|
| 17P | Request for examination filed |
Effective date: 19850507 |
|
| 17Q | First examination report despatched |
Effective date: 19860425 |
|
| ITF | It: translation for a ep patent filed | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT CH DE FR GB IT LI NL |
|
| REF | Corresponds to: |
Ref document number: 28259 Country of ref document: AT Date of ref document: 19870815 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 3464687 Country of ref document: DE Date of ref document: 19870820 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| ITTA | It: last paid annual fee | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19921015 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19921016 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 19921028 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 19921031 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 19921118 Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19931025 Ref country code: AT Effective date: 19931025 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19931031 Ref country code: CH Effective date: 19931031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19940501 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee | ||
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19931025 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19940630 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19941027 Year of fee payment: 11 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19960702 |