EP0183031A2 - Method of making holes with high-quality surface and device for carrying out the method - Google Patents
Method of making holes with high-quality surface and device for carrying out the method Download PDFInfo
- Publication number
- EP0183031A2 EP0183031A2 EP85113073A EP85113073A EP0183031A2 EP 0183031 A2 EP0183031 A2 EP 0183031A2 EP 85113073 A EP85113073 A EP 85113073A EP 85113073 A EP85113073 A EP 85113073A EP 0183031 A2 EP0183031 A2 EP 0183031A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- stroke
- honing
- reversal
- during
- cylinder
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B24—GRINDING; POLISHING
- B24B—MACHINES, DEVICES, OR PROCESSES FOR GRINDING OR POLISHING; DRESSING OR CONDITIONING OF ABRADING SURFACES; FEEDING OF GRINDING, POLISHING, OR LAPPING AGENTS
- B24B33/00—Honing machines or devices; Accessories therefor
- B24B33/06—Honing machines or devices; Accessories therefor with controlling or gauging equipment
Definitions
- the invention relates to a method according to the preamble of claim 1 and an apparatus for performing the method.
- Known methods of this type often show in practice a deterioration in the surface quality of the bore in the area in which a reversal of the direction of the stroke movement of the honing tool occurs. If one considers the preferred application of the invention, namely the production of cylinder bores, for example in engine cylinder blocks, the lifting movement is reversed when the honing tool is positioned both in the region of the end on the cylinder head side and in the region of the end of the cylinder block on the crankshaft side.
- this solution requires that the honing tool can be inserted into the cylinder bore from the crankshaft side, but this is not possible with a large number of engine blocks because of the crankshaft bearing webs.
- the known solution is not applicable in most cases.
- the invention has for its object to provide a method of the type mentioned and an apparatus for performing the method by which the described disadvantage, namely influencing the surface quality of a bore by reversing the movement of a honing tool, is avoided.
- the honing tool 5 executes an opposite stroke movement between the reversal points UT and OT (FIG. 1), which limit the size of the stroke.
- the honing stones 9 (FIG. 2) of the honing tool are pressed against the wall 10 of the cylinder bore of a cylinder to be honed or the like with a certain force (pressing force).
- the speed of the stroke movement is essentially constant between the reversals of the stroke, as the longer, straight sections of line 1 in the path-time diagram show.
- the cutting force interruption of the honing stones according to the invention is achieved during the reversal of the stroke by a brief reset of the delivery system or the delivery device triggered by the stroke control.
- the entire infeed system is prestressed against the infeed direction, as a result of which a particularly rapid interruption of the cutting force is achieved, as is also the case with the approximately rectangular shape of the Force characteristic curve 2 (FIG. 1) can be seen over time.
- a honing device is shown schematically in FIG.
- the cylinder bore 3 of an engine cylinder block 4 is machined by a honing tool 5 which is rotatably driven in a known manner and which executes a lifting movement H in the direction of the bore axis.
- the Hontechnikzeu g 5 is articulated for this purpose via a connecting rod 6 with a honing spindle 7, which is part of a known honing machine, not shown, and can be moved up and down by a hydraulic lifting drive, namely a piston-cylinder arrangement 8.
- the honing spindle 7 is also driven in a known manner by a rotary drive (not shown) about its longitudinal axis.
- the honing tool 5 carries honing stones 9 which can be advanced radially outwards by a hydraulically actuated delivery device and can be pressed against the bore wall 10 of a cylinder bore 3.
- the hydraulic actuation of the advancing device consists of a piston-cylinder assembly 11 whose piston rod 12 a through the honing spindle 7, the terminal Stan and g e 6 through the honing tool 5 leading multi-part feed rod 13 to the upper side of the feeding cone presses 14 of the honing tool.
- the force of a strong spring 15 presses on the underside of the feed cone in the opposite direction and causes the feed system to be mechanically preloaded.
- the hydraulic cylinder 11 is fed via lines 16, 17 from a hydraulic control unit 18 which is connected to a pressure medium source 19.
- a 3-way valve 21 interposed, via which the upper cylinder chamber 20 can be connected directly to a return line 22 to the pressure medium container 28.
- the 3-way valve 21 is connected via a control line 24 to an electrical stroke control device 25, which is mechanically connected to the stroke movement of the honing spindle 7, e.g. B. via a chain drive 26, coupled encoder 27 controls the stroke reversal.
- the stroke control device 25 also outputs a control signal 24 to the directional control valve 21 for each stroke reversal.
- the directional control valve 21 switches from the switching position 21a, in which the upper cylinder chamber 20 of the piston-cylinder arrangement 11 is fed by the hydraulic control unit 18 via the line 16 for the purpose of hydraulically actuating the delivery device, to the switching position 21b and remains in this position, as long as the control signal 24 is present.
- the directional control valve 21 switches back to the switching position 21a and the line 20 is immediately refilled via the line 16 until the preset pressure is reached and the honing stones 9 press and cut against the bore wall 10 again with the appropriate force .
- the start, duration and sequence of the control signal 24 is controlled in advance according to the invention by known electrical means of reversing the stroke so that, taking into account the existing mechanical and hydraulic delay times, the actual cutting force interruption of the honing stones 9 coincides with the beginning of the duration and sequence of the reversal of the stroke, as from the diagram (Fig. 1) is clearly visible.
- the control system is preferably designed so that the beginning of the reduction in cutting force (point C of line 2 in FIG. 1) takes place in good time so that when the stroke reversal begins (point A or B of line 1 in FIG. 1) the preset is already set reduced cutting force F O is fully reached and is maintained until the end of the stroke reversal (point A 'or B').
- the method according to the invention of at least reducing, preferably interrupting, the cutting force of the honing stones during the stroke reversal can be used for a workpiece during the entire honing period.
- the method is preferably only used during the finishing machining. It can also be quite sufficient and advantageous to use the method during at least one, preferably several, reversals of stroke before the finished dimension is reached.
- the method according to the invention is not limited to the hydraulic actuation of the delivery device described, but can be used in a suitable form for all known actuations for the delivery of the honing stones.
- the cutting force reduction according to the invention can be achieved during the reversal of the stroke by a brief reversal of the direction of rotation triggered by the stroke control.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Finish Polishing, Edge Sharpening, And Grinding By Specific Grinding Devices (AREA)
Abstract
Die Erfindung betrifft ein Verfahren sowie eine Vorrichtung zur Herstellung von Bohrungen hoher Oberflächengüte in Werkstücken, insbesondere von Zylinderbohrungen in Motorzylinderblöcken, durch zumindest eine Oberflächen-Feinbearbeitung mittels eines rotierenden, in Richtung der Achse der Bohrung gegenläufige Hubbewe gung ausführenden Honwerkzeuges (5) mit radial gegen die Bohrungswand mittels eines Zustellsystemes andrückbaren Honsteinen (9). Die Aufgabe ist, ein Verfahren und eine Vorrichtung dieser Art zu schaffen, bei welchen schädliche Beeinflussungen der Oberflächengüte einer Bohrung infolge Bewegungsumkehr des Honwerkzeuges (9) vermieden werden. Erreicht wird dies dadurch, daß die Kraft, mit der die Honsteine gegen die Bohrungswand (10) gedrückt werden, während den Umkehrungen der Hubbewegung des Honwerkzeuges (9) reduziert wird, indem bei der Vorrichtung der Druck im Zylinderraum (20) der Kolbenzylinder-Anordnung (11) während den Hubumkehrungen des Honwerkzeuges (5) vermindert wird.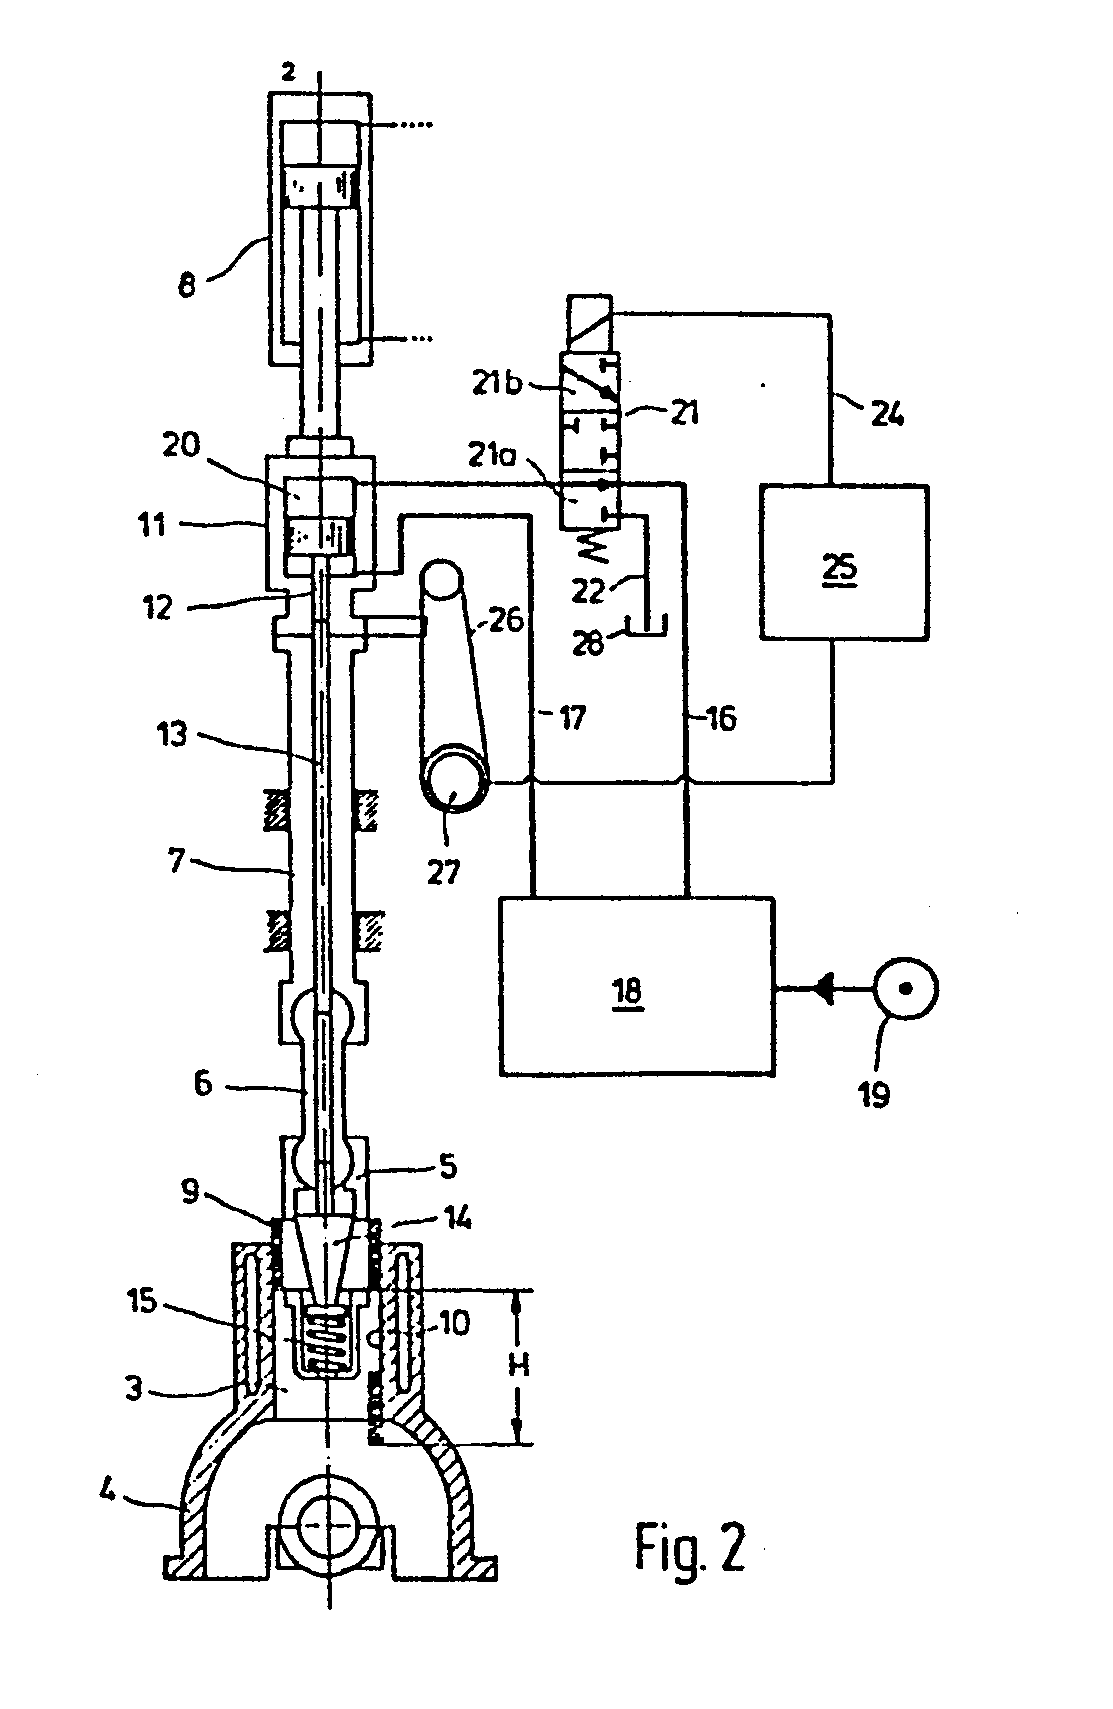
Description
Die Erfindung betrifft ein Verfahren nach dem Oberbegriff des Anspruches 1 und eine Vorrichtung zur Durchführung des Verfahrens. Bei bekannten Verfahren dieser Art zeigt sich in der Praxis häufig eine Verschlechterung der Oberflächengüte der Bohrung in dem Bereich, in dem eine Richtungsumkehr der Hubbewegung des Honwerkzeuges auftritt. Betrachtet man den bevorzugten Anwendungsfall der Erfindung, nämlich die Herstellung von Zylinderbohrungen z.B. in Motorzylinderblöcken, so erfolgen Umkehrungen der Hubbewegung bei Stellungen des Honwerkzeuges sowohl im Bereich des zylinderkopfseitigen Endes als auch im Bereich des kurbelwellenseitigen Endes des Zylinderblocks. In den Bereichen der Hubumkehr läßt sich beim Stand der Technik ein im Hinblick auf die ölhaftung und Abdichtung durch die Kolbenringe günstiger Wert des Honwinkels, also des aus Hub- und Rotationsbewegung des Werkzeuges resultierenden Winkels sich kreuzender, geradliniger Bearbeitungsriefen, nicht einhalten; in Verzögerungs-und Beschleunigungsbereichen ist der Winkel kleiner als der Sollwert, während er an den Umkehrstellen 0° beträgt. Die Oberfläche zeigt demgemäß in diesen Bereichen der Bohrung kein gleichmäßiges Bild, vielmehr sind entsprechend der Anzahl und Anordnung der in Eingriff stehenden Honsteine mehr oder weniger schmale Abschnitte mit kurzen bogenförmigen Bearbeitungsriefen vorhanden, die eine unerwünschte Verschlechterung der Oberflächengüte darstellen.The invention relates to a method according to the preamble of claim 1 and an apparatus for performing the method. Known methods of this type often show in practice a deterioration in the surface quality of the bore in the area in which a reversal of the direction of the stroke movement of the honing tool occurs. If one considers the preferred application of the invention, namely the production of cylinder bores, for example in engine cylinder blocks, the lifting movement is reversed when the honing tool is positioned both in the region of the end on the cylinder head side and in the region of the end of the cylinder block on the crankshaft side. In the areas of stroke reversal, a value of the honing angle which is favorable with regard to the oil adhesion and sealing by the piston rings, that is to say the angle of intersecting, straight machining grooves resulting from the stroke and rotational movement of the tool, cannot be maintained; in deceleration and acceleration ranges, the angle is smaller than the setpoint, while it is 0 ° at the reversal points. The surface accordingly does not show a uniform image in these areas of the bore, but rather is in accordance with the number and arrangement of the engaging honing stones present more or less narrow sections with short arcuate machining grooves, which represent an undesirable deterioration in the surface quality.
Man hat bereits versucht, die geschilderten Nachteile dadurch zu beheben, daß Motorzylinderblöcke paarweise gegensinnig mit ihren zylinderkopfseitigen Flächen aufeinander gespannt und die fluchtenden Zylinderbohrungen beider Motorblöcke wie eine Bohrung bearbeitet werden. Die schädliche Beeinflussung der Oberflächengüte kann dabei aber nur für den zylinderkopfseitigen Bereich der Zylinderbohrung vermieden werden.Attempts have already been made to remedy the disadvantages described in that engine cylinder blocks are clamped in pairs in opposite directions with their surfaces on the cylinder head side and the aligned cylinder bores of both engine blocks are machined like a bore. The deleterious influence on the surface quality can only be avoided for the area of the cylinder bore on the cylinder head side.
Außerdem erfordert diese Lösung, daß das Honwerkzeug von der Kurbelwellenseite her in die Zylinderbohrung einführbar ist, was aber bei sehr vielen Motorblöcken wegen der Kurbelwellen-Lagerstege nicht möglich ist. Die bekannte Lösung ist in den meisten Fällen nicht anwendbar.In addition, this solution requires that the honing tool can be inserted into the cylinder bore from the crankshaft side, but this is not possible with a large number of engine blocks because of the crankshaft bearing webs. The known solution is not applicable in most cases.
Der Erfindung liegt die Aufgabe zugrunde, ein Verfahren der eingangs genannten Art und eine Vorrichtung zur Durchführung des Verfahrens zu schaffen, durch welche der geschilderte Nachteil, nämlich die Beeinflussung der Oberflächengüte einer Bohrung durch Bewegungsumkehr eines Honwerkzeuges, vermieden wird.The invention has for its object to provide a method of the type mentioned and an apparatus for performing the method by which the described disadvantage, namely influencing the surface quality of a bore by reversing the movement of a honing tool, is avoided.
Diese Aufgabe wird bei dem Verfahren gemäß Gattungsbegriff des Anspruches 1 durch die Merkmale des Kennzeichens dieses Anspruches und bei einer Vorrichtung gemäß Anspruch 9 mit dessen Kennzeichnungsmerkmalen gelöst.This object is solved of claim 1 9 in the method according generic term by the characterizing features of this claim and a device according to claim ennzeichnungsmerkmalen with the K.
Durch die Herabsetzung des Hondruckes und damit der Schnittkraft des Hcnsteines in den Bereichen der Hubumkehr, d. h. in den Verzögerungs- und Beschleunigungsphasen der Hubbewegung, wird ein Schneiden der Honsteine während dieser Zeit vermieden, mindestens jedoch soweit vermindert, daß eine schädliche Oberflächenbeeinflussung ausgeschlossen ist.By reducing the honing pressure and thus the cutting force of the stone in the areas of the stroke reversing, ie in the deceleration and acceleration phases of the lifting movement, cutting of the honing stones is avoided during this time, but at least reduced to the extent that a harmful surface influence is excluded.
Weitere Merkmale der Erfindung ergeben sich aus der Beschreibung eines Ausführungsbeispieles in Verbindung und der Zeichnung und aus den Unteransprüchen.
- Fig. 1 zeigt zur Erläuterung des erfindungsgemäßen Verfahrens ein Weg(s)-Zeit(t)-Diagramm der Hubbewegung eines Honwerkzeuges mit dem zugeordneten Verlauf der Schnittkraft (F) der Honsteine während eines Abschnittes der Bearbeitung einer Bohrung und
- Fig. 2 zeigt ein Ausführungsbeispiel einer Vorrichtung zur Durchführung des Verfahrens.
- 1 shows a path (s) -time (t) diagram of the lifting movement of a honing tool with the associated course of the cutting force (F) of the honing stones during a section of the machining of a bore and to explain the method according to the invention
- Fig. 2 shows an embodiment of an apparatus for performing the method.
Das Honwerkzeug 5 (Fig. 2) führt eine gegenläufige Hubbewegung zwischen den Umkehrpunkten UT und OT (Fig. 1) aus, welche die Größe des Hubweges begrenzen. Dabei werden die Honsteine 9 (Fig. 2) des Honwerkzeuges gegen die Wandung 10 der Zylinderbohrung eines zu honenden Zylinders oder dgl. mit einer bestimmten Kraft (Andruckkraft) gedrückt. Die Geschwindigkeit der Hubbewegung ist zwischen den Hubumkehrungen im wesentlichen konstant, wie die längeren, geraden Abschnitte der`Linie 1 im Weg-Zeit-Diagramm zeigen.The honing tool 5 (FIG. 2) executes an opposite stroke movement between the reversal points UT and OT (FIG. 1), which limit the size of the stroke. The honing stones 9 (FIG. 2) of the honing tool are pressed against the
Im Punkt A wird die Umkehr der Hubbewegung eingeleitet, d. h. die bewegten Massen müssen bis zum Stillstand abgebremst und unmittelbar in entgegengesetzter Richtung wieder beschleunigt werden. Der bogenförmige Verlauf der Linie 1 in diesem Bereich zeigt, daß sich die Geschwindigkeit schnell verringert und im Umkehrpunkt UT den Wert Null erreicht (Scheitelpunkt der Kurve), dann rasch wieder zunimmt, um im Punkt A' die Arbeitshubgeschwindigkeit wieder zu erreichen. Das gleiche gilt für die Hubumkehr am oberen Umkehrpunkt OT, die durch die Punkte B und B' markiert ist.At point A, the reversal of the lifting movement is initiated, i. H. the moving masses must be braked to a standstill and immediately accelerated in the opposite direction. The arcuate course of line 1 in this area shows that the speed decreases rapidly and reaches zero at the reversal point UT (apex of the curve), then increases again rapidly to reach the working stroke speed again at point A '. The same applies to the stroke reversal at the upper reversal point OT, which is marked by points B and B '.
Das in Fig. 1 dargestellte Diagramm zeigt weiter im unteren Teil mit der Linie 2 den erfindungsgemäßen, der Hubbewegung zugeordneten Verlauf der Andruckkraft der Honsteine an die Bohrungswand über der Zeit. Es ist deutlich zu sehen, daß im bogenförmigen Bereich der Linie 1 zwischen Punkt A und A' bzw. B und B' die Honkraft schlagartig von F1 auf F0 vermindert wird, vorzugsweise auf F0=0 herabgesetzt wird. Das bedeutet, daß in der Verzögerungs- und Beschleunigungsphase des Honwerkzeuges, also während der Hubumkehr, die Honsteine nicht mehr schneiden können und keine Bearbeitungsriefen erzeugen.The diagram shown in FIG. 1 further shows in the lower part with
Erreicht wird die erfindungsgemäße Schnittkraftunterbrechung der Honsteine während der Hubumkehr durch eine von der Hubsteuerung ausgelöste kurzzeitige Rückstellung des Zustellsystems bzw. der Zustelleinrichtung.The cutting force interruption of the honing stones according to the invention is achieved during the reversal of the stroke by a brief reset of the delivery system or the delivery device triggered by the stroke control.
Hierzu ist nach einem weiteren Merkmal der Erfindung das gesamte Zustellsystem entgegen der Zustellrichtung vorgespannt, wodurch eine besonders schnell einsetzende Schnittkraftunterbrechung erreicht wird, wie dies auch aus dem angenähert rechteckförmigen Verlauf der Kraftkennlinie 2 (Fig. 1) über der Zeit ersichtlich ist.For this purpose, according to a further feature of the invention, the entire infeed system is prestressed against the infeed direction, as a result of which a particularly rapid interruption of the cutting force is achieved, as is also the case with the approximately rectangular shape of the Force characteristic curve 2 (FIG. 1) can be seen over time.
In Fig. 2 ist schematisch eine erfindungsgemäße Honvorrichtung dargestellt. Die Zylinderbohrung 3 eines Motorzylinderblockes 4 wird von einem in bekannter Weise rotierend angetriebenen und eine in Richtung der Bohrungsachse eine Hubbewegung H ausführenden Honwerkzeug 5 bearbeitet.A honing device according to the invention is shown schematically in FIG. The
Das Honwerkzeug 5 ist zu diesem Zweck über eine Anschlußstange 6 gelenkig mit einer Honspindel 7 verbunden, die Teil einer nicht gezeigten bekannten Honmaschine ist und von einem hydraulischen Hubantrieb, nämlich einer Kolbenzylinder-Anordnung 8 nach oben und unten bewegbar ist. Die Honspindel 7 wird außerdem in bekannter Weise von einem (nicht gezeigten) Drehantrieb um ihre Längsachse drehend angetrieben. Das Honwerkzeug 5 trägt Honsteine 9, die von einer hydraulisch betätigten Zustelleinrichtung radial nach außen zustell-und an die Bohrungswand 10 einer Zylinderbohrung 3 andrückbar sind. Die hydraulische Betätigung der Zustelleinrichtung besteht aus einer Kolbenzylinder-Anordnung 11, deren Kolbenstange 12 über eine durch die Honspindel 7 und die Anschlußstange 6 hindurch zum Honwerkzeug 5 führende, mehrteilig ausgeführte Zustellstange 13 auf die Oberseite des Zustellkonus 14 des Honwerkzeuges drückt. Auf die Unterseite des Zustellkonus drückt die Kraft einer starken Feder 15 in entgegengesetzter Richtung und bewirkt eine mechanische Vorspannung des Zustellsystems. Der hydraulische Zylinder 11 wird über Leitungen 16, 17 von einer hydraulischen Steuereinheit 18 gespeist, die an eine Druckmittelquelle 19 angeschlossen ist.The Honwerkzeu g 5 is articulated for this purpose via a connecting
In die Leitung 16, welche zum oberen Zylinderraum 20 der Kolbenzylinder-Anordnung 11 führt, ist ein 3-Wege-Ventil 21 zwischengeschaltet, über das der obere Zylinderraum 20 direkt mit einer Rücklaufleitung 22 zum Druckmittelbehälter 28 verbindbar ist. Das 3-Wege-Ventil 21 ist über eine Steuerleitung 24 mit einem elektrischen Hubsteuergerät 25 verbunden, das mittels eines mit der Hubbewegung der Honspindel 7 mechanisch, z. B. über einen Kettentrieb 26, gekoppelten Weggebers 27 die Hubumkehr steuert.In the
Die in Fig. 2 beschriebene Vorrichtung arbeitet wie folgt:
- Der über den
Kettentrieb 26 mit der auf- undabbewegten Honspindel 7verbundene Weggeber 27 arbeitet als Istwertgeber und meldet fortlaufend die augenblickliche Stellung desHonwerkzeuges 5 an dasHubsteuergerät 25. ImHubsteuergerät 25 werden in bekannter Weise diese Werte mit vorgegebenen Sollwerten für die Hubumkehrpunkte (UT, OT) verglichen und bei Gleichheit die Hubumsteuerung bewirkt.
- The
displacement sensor 27 connected to thehoning spindle 7 moved up and down via thechain drive 26 works as an actual value transmitter and continuously reports the instantaneous position of thehoning tool 5 to thestroke control device 25 , OT) are compared and the stroke reversal is effected if they are the same.
Das Hubsteuergerät 25 gibt außerdem erfindungsgemäß zu jeder Hubumsteuerung ein Steuersignal 24 an das Wegeventil 21 ab. Das Wegeventil 21 steuert aus der Schaltstellung 21a, in welcher der obere Zylinderraum 20 der Kolbenzylinder-Anordnung 11 zum Zwecke der hydraulischen Betätigung der Zustelleinrichtung über die Leitung 16 von der hydraulischen Steuereinheit 18 gespeist ist, in die Schaltstellung 21b um und verbleibt in dieser Stellung, solange das Steuersignal 24 ansteht.The
In der Schaltstellung 21b ist die Leitung 16 zur hydraulischen Steuereinheit 18 unterbrochen. Der Zylinderraum 20 ist jetzt mit der Rücklaufleitung 22 verbunden, und aus dem Zylinderraum 20 strömt Druckmittel zurück in den Behälter 28. Der Druck im Zylinderraum 20, der maßgebend ist für die Kraft, mit der die Honsteine 9 beim Honen gegen die Bohrungswand 10 gedrückt werden, fällt schlagartig ab und die Vorspannfeder 15 bewirkt eine schnelle Rückstellung des Zustellsystems; die Honsteine 9 werden nicht mehr gegen die Bohrungswand 10 gedrückt und hören sofort auf zu schneiden.In the
Nach Wegnahme des Signals 24 schaltet das Wegeventil 21 zurück in die Schaltstellung 21a und über die Leitung 16 erfolgt sofort wieder die Auffüllung des Zylinderraums 20, bis der voreingestellte Druck erreicht ist und die Honsteine 9 wieder mit der entsprechenden Kraft gegen die Bohrungswand 10 drücken und schneiden.After the
Beginn, Dauer und Folge des Steuersignals 24 wird erfindungsgemäß durch an sich bekannte elektrische Mittel der Hubumkehr vorauseilend so gesteuert, daß unter Berücksichtigung der vorhandenen mechanischen und hydraulischen Verzögerungszeiten die tatsächliche Schnittkraftunterbrechung der Honsteine 9 mit dem Anfang der Zeitdauer und Folge der Hubumkehr übereinstimmt, wie aus dem Diagramm (Fig. 1) gut erkennbar ist. Dabei ist die Steuerung vorzugsweise so ausgelegt, daß der Beginn der Schnittkraftverminderung (Punkt C der Linie 2 in Fig. 1) so rechtzeitig erfolgt, daß beim Beginn der Hubumkehr ( Punkt A bzw. B der Linie 1 in Fig. 1) bereits die voreingestellte verminderte Schnittkraft FO voll erreicht ist und bis zum Ende der Hubumkehr (Punkt A' bzw. B') aufrechterhalten wird.The start, duration and sequence of the
Das erfindungsgemäße Verfahren, die Schnittkraft der Honsteine während der Hubumkehr mindestens zu reduzieren, vorzugsweise zu unterbrechen, kann während der gesamten Hondauer für ein Werkstück angewendet werden.The method according to the invention of at least reducing, preferably interrupting, the cutting force of the honing stones during the stroke reversal can be used for a workpiece during the entire honing period.
Bei mehrstufiger Bearbeitung wird das Verfahren vorzugsweise nur während der Fertigbearbeitung angewendet. Es kann auch durchaus genügen und vorteilhaft sein, während mindestens einer, vorzugsweise mehrerer, Hubumkehrungen vor Erreichen des Fertigmaßes das Verfahren anzuwenden.In the case of multi-stage machining, the method is preferably only used during the finishing machining. It can also be quite sufficient and advantageous to use the method during at least one, preferably several, reversals of stroke before the finished dimension is reached.
Selbstverständlich ist das erfindungsgemäße Verfahren nicht auf die beschriebene hydraulische Betätigung der Zustelleinrichtung beschränkt, sondern kann bei allen bekannten Betätigungen für die Zustellung der Honsteine in geeigneter Form angewendet werden.Of course, the method according to the invention is not limited to the hydraulic actuation of the delivery device described, but can be used in a suitable form for all known actuations for the delivery of the honing stones.
So kann beispielsweise bei einer elektro-mechanischen Betätigung der Zustelleinrichtung mittels Schritt-oder Servomotor in Verbindung mit einem Kugelgewindetrieb durch eine kurzzeitige, von der Hubsteuerung ausgelöste Drehrichtungsumkehr die erfindungsgemäße Schnittkraftverminderung während der Hubumkehr erreicht werden.For example, when the delivery device is actuated electromechanically by means of a stepping or servo motor in conjunction with a ball screw drive, the cutting force reduction according to the invention can be achieved during the reversal of the stroke by a brief reversal of the direction of rotation triggered by the stroke control.
Claims (11)
durch zumindest eine Oberflächen-Feinbearbeitung mittels eines rotierenden, in Richtung der Achse der Bohrung gegenläufige Hubbewegung ausführenden Honwerkzeuges mit radial gegen die Bohrungswand mittels eines Zustellsystems andrückbaren Honsteinen,
dadurch gekennzeichnet, daß die Kraft, mit der die Honsteine (9) gegen die Bohrungswand (10) gedrückt werden, während den Umkehrungen der Hub- bewegung des Honwerkzeuges (5) reduziert wird.1. Process for producing high-quality surface bores in workpieces, in particular cylinder bores in engine cylinder blocks,
by at least one surface finishing by means of a rotating honing tool which executes a reciprocating stroke movement in the direction of the axis of the bore with honing stones which can be pressed radially against the bore wall by means of a feed system,
characterized in that the force with which the honing stones are pushed (9) against the bore wall (10), during the movement reversals of the H UB honing tool is reduced (5).
dadurch gekennzeichnet, daß die Kraft, mit der die Honsteine (9) gegen die Bohrungswand (10) gedrückt werden, während den Umkehrungen der Hubbewegung des Honwerkzeuges (5) auf Null herabgesetzt wird.2. The method according to claim 1,
characterized in that the force with which the honing stones (9) are pressed against the bore wall (10) is reduced to zero during the reversals of the lifting movement of the honing tool (5).
dadurch gekennzeichnet, daß eine Schnittkraftverminderung der Honsteine (9) während der Hubumkehr durch eine von einer Hubsteuerung (25) ausgelöste Rückstellung des Zustellsystems vorgenommen wird.3. The method according to claim 1 or 2,
characterized in that a cutting force reduction of H onsteine (9) during the stroke reversal by a triggered by a lift control (25) resetting the Z ustellsystems is made.
dadurch gekennzeichnet, daß die Schnittkraftverminderung der Honsteine (9) bei der Hubumkehr während der gesamten Hondauer für ein Werkstück vorzugsweise bei der Hubumkehr während der Fertigbearbeitung eines Werkstückes angewendet wird.6. The method according to any one of claims 1 to 5,
characterized in that the reduction in the cutting force of the honing stones (9) is used for reversing the stroke during the entire honing period for a workpiece, preferably for reversing the stroke during the finishing of a workpiece.
dadurch gekennzeichnet, daß die Schnittkraftunterbrechung der Honsteine bei derHubumkehrwährend mindestens einer, vorzugsweise mehrerer Hubumkehrungen vor Erreichen des Fertigmaßes angewendet wird.7. The method according to any one of claims 1 to 6,
characterized in that the cutting force interruption of the honing stones is applied during the stroke reversal during at least one, preferably several stroke reversals before the finished dimension is reached.
dadurch gekennzeichnet, daß das Zustellsystem mit einer entgegen der Zustellrichtung wirkenden Vorspanneinrichtung versehen ist, vorzugsweise einer Druckfeder (15), die auf die Unterseite des Zustellkonus (14) des Honwerkzeuges (5) drückt.9. The device according to claim 8,
characterized in that the infeed system is provided with a prestressing device acting counter to the infeed direction, preferably a compression spring (15) which presses on the underside of the infeed cone (14) of the honing tool (5).
dadurch gekennzeichnet, daß das Zustellsystem durch eine Druckfeder (15) rückstellbar ist, wobei der Zylinderraum (20) mit einer zum Druckmittelbehälter (28) führenden RückJaufleitung (22) verbunden ist.10. The device according to claim 8 or 9,
characterized in that the delivery system can be reset by a compression spring (15), the cylinder space (20) being connected to a return line (22) leading to the pressure medium container (28).
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19843443106 DE3443106A1 (en) | 1984-11-27 | 1984-11-27 | METHOD FOR PRODUCING BORES OF HIGH SURFACE QUALITY AND DEVICE FOR CARRYING OUT THE METHOD |
| DE3443106 | 1984-11-27 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0183031A2 true EP0183031A2 (en) | 1986-06-04 |
| EP0183031A3 EP0183031A3 (en) | 1987-12-16 |
| EP0183031B1 EP0183031B1 (en) | 1991-07-24 |
Family
ID=6251201
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP85113073A Expired - Lifetime EP0183031B1 (en) | 1984-11-27 | 1985-10-15 | Method of making holes with high-quality surface and device for carrying out the method |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US4683680A (en) |
| EP (1) | EP0183031B1 (en) |
| JP (1) | JPS61131864A (en) |
| DE (2) | DE3443106A1 (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN111843813A (en) * | 2020-06-29 | 2020-10-30 | 西安理工大学 | A hydraulic driven internal combustion engine cylinder bore machining honing head and its hydraulic circuit |
Families Citing this family (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5191864A (en) * | 1992-02-03 | 1993-03-09 | Briggs & Stratton Corporation | Engine cylinder bore |
| US6095907A (en) * | 1998-10-02 | 2000-08-01 | Kennametal Inc. | Reciprocating assembly for abrading a workpiece |
| US6962279B1 (en) * | 2000-10-18 | 2005-11-08 | Ge Medical Systems Global Technology Company, Llc | Apparatus and method for glass separation for flat panel displays |
| US6786807B2 (en) | 2002-09-03 | 2004-09-07 | Micromatic Operations, Inc. | Universal coupling for machine tool |
| DE202008012092U1 (en) | 2008-09-08 | 2010-02-11 | Gehring Technologies Gmbh | Device for arranging a honing tool on a honing machine |
| DE102013220507B4 (en) * | 2013-10-11 | 2015-11-05 | Gehring Technologies Gmbh | Apparatus and method for producing a non-cylindrical inner surface of a bore |
| DE102014210012A1 (en) * | 2014-05-26 | 2015-11-26 | Elgan-Diamantwerkzeuge Gmbh & Co. Kg | Honing process for fine machining of holes |
| JP7500201B2 (en) * | 2020-01-15 | 2024-06-17 | トーヨーエイテック株式会社 | Honing device and processing method using same |
| CN114473837B (en) * | 2021-12-27 | 2025-02-11 | 湖北利锐特精密机电设备有限公司 | A vertical honing machine loading stand |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2403546A (en) * | 1943-09-27 | 1946-07-09 | Barnes Drill Co | Method and apparatus for honing |
| GB761086A (en) * | 1953-08-19 | 1956-11-07 | Barnes Drill Co | Fluid pressure gauge for use with honing tools |
| US3466809A (en) * | 1967-06-07 | 1969-09-16 | Barnes Drill Co | Machine tool traverse control |
| JPS5629091Y2 (en) * | 1978-10-03 | 1981-07-10 | ||
| JPS5676376A (en) * | 1979-11-22 | 1981-06-23 | Fujikoshi Kikai Kogyo Kk | Correction of platen of lapping apparatus and lapping apparatus therefore |
| DE3039467A1 (en) * | 1980-10-18 | 1982-06-03 | Maschinenfabrik Gehring Gmbh & Co Kg, 7302 Ostfildern | HONING MACHINE FOR MACHINING WORK PIECE BORES, ESPECIALLY BAG HOLES AND METHOD FOR OPERATING THE HONING MACHINE |
| GB2111876A (en) * | 1981-12-09 | 1983-07-13 | Jones & Shipman Plc | Improvements relating to honing |
-
1984
- 1984-11-27 DE DE19843443106 patent/DE3443106A1/en active Granted
-
1985
- 1985-10-15 DE DE8585113073T patent/DE3583584D1/en not_active Expired - Fee Related
- 1985-10-15 EP EP85113073A patent/EP0183031B1/en not_active Expired - Lifetime
- 1985-11-26 JP JP60263965A patent/JPS61131864A/en active Granted
- 1985-11-27 US US06/802,857 patent/US4683680A/en not_active Expired - Fee Related
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN111843813A (en) * | 2020-06-29 | 2020-10-30 | 西安理工大学 | A hydraulic driven internal combustion engine cylinder bore machining honing head and its hydraulic circuit |
Also Published As
| Publication number | Publication date |
|---|---|
| DE3443106C2 (en) | 1992-09-17 |
| EP0183031A3 (en) | 1987-12-16 |
| DE3443106A1 (en) | 1986-06-05 |
| JPS61131864A (en) | 1986-06-19 |
| DE3583584D1 (en) | 1991-08-29 |
| US4683680A (en) | 1987-08-04 |
| EP0183031B1 (en) | 1991-07-24 |
| JPH0364271B2 (en) | 1991-10-04 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0418779B1 (en) | Method for manufacture of workpieces by punching, in particular in a precision counter punching tool | |
| EP0321590B1 (en) | Method and device for manufacturing a cutting die having a sharp cutting edge | |
| DE3012486A1 (en) | DEVICE LIKE A PUNCH OR PRESS | |
| EP0017660A1 (en) | Hydraulic press | |
| DE3443106C2 (en) | ||
| DE2065754A1 (en) | MOTION CONVERSION DEVICE | |
| DE1948119A1 (en) | Device for chamfering the edges of a toothed workpiece | |
| DE2430608A1 (en) | METHOD AND DEVICE FOR PERFORMING THE METHOD FOR CUTTING WORK PIECES OF CERTAIN LENGTH OF PROFILE MATERIAL, E.G. FROM A PIPE | |
| DE2165247A1 (en) | DEVICE AND METHOD FOR SEPARATING TUBULAR BLANKS | |
| EP0144786A1 (en) | Separation device | |
| DE2604858A1 (en) | METHOD AND DEVICE FOR REGULATING THE WORKING PRESSURE OF A HYDRAULIC MEDIUM SUPPORTED TO A PISTON UNIT | |
| DE2432774A1 (en) | METHOD FOR CONTROLLING THE FORWARD AND RETURN FLOW OF A TOOL ON A MACHINE AND DEVICE FOR EXECUTING THE METHOD | |
| DE2458366A1 (en) | GRINDING PROCESS AND DEVICE FOR IMPLEMENTING THIS PROCESS | |
| DE2657357A1 (en) | METHOD AND DEVICE FOR ELECTROEROSIVE MACHINING | |
| EP0133254A2 (en) | Method and apparatus for calibrating, deforming and compressing the surfaces of tubes | |
| DE2334667A1 (en) | External honing tool with guided support - support feed movement is limited by stop nuts on each feed spindle | |
| DE3703848A1 (en) | Device for advancing a honing tool | |
| DE69404792T2 (en) | Rod sharpening machine | |
| DE2537030C3 (en) | Device for cutting metals, preferably steel bars, at increased cutting speeds into sections of exact shape and length | |
| WO1998031941A1 (en) | Device for controlling a cylinder | |
| DE2423177A1 (en) | DEVICE FOR ADJUSTING AND ALIGNING THE CONTAINERS OF AN EXTRUSION PRESS | |
| DE1165969B (en) | Feed device for moving cutting machines | |
| DE2438784A1 (en) | Rolling head to profile cylindrical work pieces - uses hydraulically or pneumatically driven actuator | |
| DE19642437A1 (en) | Press for forming workpieces from powdered ceramic clay | |
| DE1959557C3 (en) | Block and slab shears or the like. Machine tools such as presses |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): DE FR GB IT |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): DE FR GB IT |
|
| 17P | Request for examination filed |
Effective date: 19880426 |
|
| RAP3 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: MASCHINENFABRIK GEHRING GMBH & CO |
|
| 17Q | First examination report despatched |
Effective date: 19890714 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB IT |
|
| ET | Fr: translation filed | ||
| REF | Corresponds to: |
Ref document number: 3583584 Country of ref document: DE Date of ref document: 19910829 |
|
| ITF | It: translation for a ep patent filed | ||
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19920929 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19921016 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19921223 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19931015 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19931015 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19940630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19940701 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |