EP0201788A2 - Dispositif pour couper et/ou rainurer des bandes de papier - Google Patents
Dispositif pour couper et/ou rainurer des bandes de papier Download PDFInfo
- Publication number
- EP0201788A2 EP0201788A2 EP86105798A EP86105798A EP0201788A2 EP 0201788 A2 EP0201788 A2 EP 0201788A2 EP 86105798 A EP86105798 A EP 86105798A EP 86105798 A EP86105798 A EP 86105798A EP 0201788 A2 EP0201788 A2 EP 0201788A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- shaft
- tool
- magnet arrangements
- arrangements
- magnet
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 239000000696 magnetic material Substances 0.000 claims abstract description 13
- 239000011111 cardboard Substances 0.000 claims abstract description 4
- 239000000123 paper Substances 0.000 claims abstract description 3
- 230000005284 excitation Effects 0.000 claims description 3
- 230000000712 assembly Effects 0.000 claims 1
- 238000000429 assembly Methods 0.000 claims 1
- 239000004020 conductor Substances 0.000 description 6
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 description 2
- 229910000831 Steel Inorganic materials 0.000 description 2
- 238000013461 design Methods 0.000 description 2
- 238000012544 monitoring process Methods 0.000 description 2
- 239000010959 steel Substances 0.000 description 2
- 238000004804 winding Methods 0.000 description 2
- 229910001369 Brass Inorganic materials 0.000 description 1
- 239000000956 alloy Substances 0.000 description 1
- 229910045601 alloy Inorganic materials 0.000 description 1
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 1
- 229910052782 aluminium Inorganic materials 0.000 description 1
- 238000013459 approach Methods 0.000 description 1
- 239000010951 brass Substances 0.000 description 1
- 239000000969 carrier Substances 0.000 description 1
- 238000006073 displacement reaction Methods 0.000 description 1
- 239000003999 initiator Substances 0.000 description 1
- 229910052742 iron Inorganic materials 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 239000011087 paperboard Substances 0.000 description 1
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D7/00—Details of apparatus for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D7/26—Means for mounting or adjusting the cutting member; Means for adjusting the stroke of the cutting member
- B26D7/2614—Means for mounting the cutting member
- B26D7/2621—Means for mounting the cutting member for circular cutters
Definitions
- Devices for the longitudinal cutting and longitudinal creasing of paper or cardboard webs normally have at least one pair of rollers with annular cutting or creasing tools in order to cut or creasing the continuous web in the longitudinal direction.
- the positions of the tools on the shafts must be readjusted.
- the tools can be clamped on the shafts and can be detached again if necessary.
- the loosening and clamping of the tools should, if possible, be carried out automatically.
- the waves as expanding waves, which are expanded radially with the aid of a pressure medium - (DE-OS 22 50 508).
- expandable hoses in the grooves of the shafts in order to clamp the tools.
- the grooves are either ring-shaped or helical.
- the positioning of the ring-shaped tools on the shaft should also be carried out automatically if possible. It is known to do this with the aid of pawls or the like, which are arranged on a threaded spindle parallel to the tool shaft and can be brought into engagement with the tools in order to shift them by a certain amount on the tool shaft (DE-PS 25 26 599). In the known device, initiators are also provided to report the positions of the tools on the tool shaft or to control the positioning process.
- the loosening and re-tightening as well as the positioning of the tools requires a certain amount of time in the known devices.
- the invention has for its object to provide a device for cutting and / or creasing cardboard or paper webs with which the tightening or loosening of the tools from the tool shaft and possibly also the positioning can be accelerated.
- This object is achieved in that the ring-shaped tool consists at least partially of magnetic material, the shaft consists of a non-magnetic material and a number of magnet arrangements, preferably at equal intervals, are arranged in the shaft, which interact magnetically with the tool and it hold in an occupied position by magnetic attraction.
- the basic idea of the invention is to generate a magnetic field on the shaft at a desired axial circumferential location, which holds the tool in the assumed position.
- the magnetic holding force must be so great that the lateral forces that occur during operation do not lead to a displacement of the tool.
- two knives or creasing tools work together.
- the knives can be biased against one another during magnetic holding, so that the certainty that the position assumed remains in place is increased.
- individual electromagnet arrangements are arranged in the shaft, which can optionally be connected to a current source outside the shaft.
- the tools can, at least partially, consist of steel or iron, and thus develop magnetic behavior in the case of a direct field.
- the electromagnets can also be operated with alternating current.
- a current can be generated in a ring-shaped conductor on the tool or tool carrier, which in turn results in a magnetic field that interacts with the magnetic field of the electromagnet (if tools are mentioned below, the arrangement of tool carriers plus is in principle actual tool).
- the tool carrier made of layered magnetic material in the form of a laminated core is necessary in order to obtain a clearly directed magnetic flow in relation to the conductor.
- the axial extent of a magnet arrangement in the shaft cannot be chosen to be arbitrarily small.
- the tools should take any position on the shaft if possible.
- one embodiment of the invention provides that the magnet arrangements are arranged in such a way that their fields overlap on the outside of the shaft.
- the power source located outside the shaft only needs to be coupled to the shaft via a pair of slip rings.
- Each magnet arrangement can optionally be assigned its own switch in the shaft, by means of which the magnet arrangements can be connected to the current source.
- a control device is provided for the optional connection of the electromagnet arrangements to the power source.
- the current source lying outside the shaft is then also connected to the shaft via slip rings.
- the switches located within the shaft are all coupled to the terminals connected to the slip rings. If a switch is closed, it connects the associated electromagnet arrangement to the power source.
- the switches can be controlled contactless or contact-based. In the latter case, an additional galvanic connection must be created from the inside of the shaft to the outside via slip rings. In order to achieve a desired magnetic field distribution on the outside of the shaft, the current flowing into a magnet arrangement can be changed if possible.
- the tool is only held magnetically.
- the tool supports at least one shoe which is radially movable with respect to the shaft axis, which is designed as an armature and which can be brought into engagement with the shaft by the magnetic field of one or more magnet arrangements.
- all magnet arrangements in the shaft can be switched on simultaneously for clamping the tool.
- a targeted control of individual magnet arrangements is therefore not necessary.
- the use of one or more of such shoes for the tool has the advantage that the tool can be relatively easily slidably mounted on the shaft.
- the magnet arrangements serve only to hold the tools in predetermined positions on the shaft.
- the positioning is carried out in any known manner.
- an arrangement comprising a plurality of electromagnets in the shaft can also be used for positioning.
- an embodiment of the invention provides that the magnet arrangements are arranged and can be connected to the power source via a control device such that a linear motor is formed in which the shaft with the magnet arrangements is the stator and the tool is the rotor.
- the basic principle of an electric linear motor is that a series of magnetic poles is provided in a linear arrangement and a rotor interacts with the magnetic poles, which rotor is carried along by a magnetic field generated by the individual poles.
- linear motors a distinction is made between AC and DC linear motors. Both are applicable to the present case.
- the field of excitation is changed in terms of time and location. As a result, a tool captured by the magnetic field of a pole can be taken along and moved on the shaft. Once it has reached the desired position, the excitation of the magnetic field is ended.
- a linear motor of this type can be used directly for positioning without the need for appropriate feedback.
- position transmitters can also be provided, which are activated in accordance with the desired position of the tool on the shaft and cause de-excitation of the electromagnet arrangements as soon as the tool has reached the desired position.
- alternating current With the help of alternating current, a moving linear field can be generated accordingly.
- this principle corresponds to the asynchronous motor developed in one plane, the tool forming the squirrel-cage rotor in the present case.
- the tool must be provided with a laminated core in order, as already explained above, to obtain a clearly directed flow and a conclusion for the magnetic field.
- the individual magnet arrangements serve as positioning devices for one or more tools.
- the magnet arrangements can be controlled in the manner described above.
- the clamping of the tools on the shaft can, however, take place in a conventional manner, for example with the aid of the pressure hoses mentioned embedded in the shaft or by expanding hoses in the tools.
- the shaft is designed as a linear motor
- the tool is simultaneously magnetically held at a standstill. After the tool has reached the desired point through the linear motor. the field remains in the area of this position in order to generate a sufficient magnetic holding force.
- the tools are preferably arranged in a rotationally fixed manner on the shaft.
- the shaft can have a continuous groove or a continuous strip parallel to this axis, which cooperates with a corresponding projection or corresponding groove on the tool.
- the pawls disclosed in DE-PS 25 26 599 are placed in the tool shaft.
- the tool shaft can have one or more pawls which are mounted in corresponding axially parallel slots and which are connected to the rotor of a linear motor.
- the pawls can also be used to secure the axial position of the tools.
- the pawls can also be moved into the tool shaft when the tools have reached their position. The tools can then be clamped onto the shaft in another way, for example according to one of the embodiments described above.
- FIG. 1 shows a frame 30 of a longitudinal cutting and creasing machine, which supports two tool shafts 31, 32 in a known manner (details are not discussed here. Reference is made, for example, to the detailed description of DE-PS 25 26 599). .
- the tool shafts 31, 32 support pairs of tools from the upper tool 33 and lower tool 34, which in the released state can be moved along the axis.
- An adjustment spindle 35 is mounted in the frame 30 above the upper tool shaft 31.
- a second adjusting spindle 36 is mounted in the frame 30 below the lower tool shaft 32.
- the shafts 31, 32 are driven synchronously by the motor 37 via a gear 38 and a gear chain 39.
- the adjusting spindles 35, 36 are driven synchronously by the motor 40 via a gear 41 and a gear chain 42.
- Slides 43 and 44 are seated on the adjusting spindles 35, 36 and are provided with a pawl 45 and 46, respectively.
- the pawl 45 or 46 can either be engaged or disengaged from a tool 33, 34. With the help of the slide 43, 44, each tool 33, 34 can be brought into any position on the tool shaft 31, 32. During operation, the pawls 45, 46 are disengaged from the tools 33, 34.
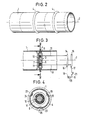
- FIG. 2 shows a tool shaft 1, which corresponds approximately to the tool shaft 31 or 32 according to FIG. 1. It is formed in the form of a ring cylinder and consists of a non-magnetic material, for example a hard aluminum or brass alloy, or of a non-magnetic steel.
- two tools 4 are also arranged extremely schematically, which can correspond to tools 33 and 34 according to FIG. 1.
- Fig. 3 shows in longitudinal section a part of the shaft of Fig. 2. It can be seen that an electro-magnet arrangement 3 is arranged within the shaft, which has two spaced disks 7, 8 made of magnetic material, which is arranged on both sides of a core 10 to which is wrapped around a winding 11.
- the discs 7, 8 are tapered at the ends, so that the discs 7, 8 approach radially outwards.
- a number of such magnet arrangements 3 is arranged close to each other. These magnet arrangements 3 can optionally be magnetically insulated from one another.
- the winding 11 is connected via two conductors 12, 13 to slip rings 14, 15 on the shaft 1, which are arranged concentrically to the axis 2 of the shaft 1 and rotate with it.
- Brushes 16, 17 interact with the slip rings 14, 15. Lines 18, 19 connect the brushes 16, 17 to a direct current source 20, a switch 21 being arranged in line 19.
- the magnet arrangement 3 is excited and a magnetic field is formed, the direction of which on the outer circumference of the shaft 1 in the region of the tool 4 runs approximately axially parallel. Since the tool 4 at at least partially consists of magnetic material, it is held in the position shown in FIG. 3. It should be noted that the air gap 9 between the disks 7, 8 must be larger than the air gap between the individual disks 7, 8 and the tool 4. In the illustration according to FIG. 3, all magnet arrangements 3 are parallel or in series with the power source 19 connected. If the magnet arrangements 3 are to be switched on selectively, each magnet arrangement 3 must be assigned its own switch. In the event that the switches are arranged outside the shaft 1, a slip ring pair must be provided for each magnet arrangement 3. It is therefore preferable to arrange the switches within the shaft and to switch them on from the outside without contact or galvanically using appropriate control commands.
- the shaft 1 has three grooves 23, 24, 25 equally spaced in the circumferential direction, which are formed on the circumference of the shaft 1 and extend axially parallel.
- the tool 4 has corresponding projections 26, 27, 28 which cooperate with the grooves 23, 24, 25 and secure the tool against rotation.
- a tool shaft 50 is shown in section in FIG. 5, which corresponds, for example, to the tool shaft 31 or 32 according to FIG. 1.
- a single tool 51 is arranged on the shaft, for example corresponding to tool 33 or 34 according to FIG. 1.
- a plurality of electromagnet arrangements 52 are arranged tightly packed next to one another.
- Each magnet arrangement has a cylindrical ring 53 made of magnetic material, into which a rectangular groove 54 is formed on the circumference.
- An electrically insulated conductor 45 of rectangular cross section is arranged in the groove 54.
- Thin disks 56 made of non-magnetic material are arranged between the disks 53.
- the conductors 55 generate a field which surrounds the conductors in a circle and pass through the tool 51 accordingly. If this is magnetic, it is held in the assumed position.
- One or more radially movably mounted shoes can be arranged in the tool 51, as shown in dashed lines at 57. When a magnet arrangement 52 is excited, the shoe 57 is pressed in the direction of the circumference of the shaft 50 in order to firmly clamp the tool 51.
- the magnet arrangements 3 according to FIG. 3 or 52 according to FIG. 5 can also be used to generate a magnetic traveling field which moves axially parallel on the outside of the shaft.
- the series arrangement of the magnet arrangements 3 or 52 is the stator of a linear motor, while the tools form the rotor.
- the magnet arrangements 3, 52 can therefore alternatively also be used to position the tools 4 or 51, as a modification of the tool positioning, as shown in FIG. 1.
- the Unearmotor formed in this way can also generate sufficient magnetic holding force in addition to the positioning to hold the tools in the assumed position.
- Position sensors can be provided for controlling and / or monitoring the position of the tools. In Fig. 6, three position sensors 48 are shown, which with a suitable control or. Monitoring circuit (not shown) are connected. The position of the pawl 45 for adjusting the tools 33 is to be determined with them so that the positioning can be carried out or monitored.
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Forests & Forestry (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Press Drives And Press Lines (AREA)
- Nonmetal Cutting Devices (AREA)
- Dynamo-Electric Clutches, Dynamo-Electric Brakes (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE8512877U | 1985-05-02 | ||
| DE19858512877 DE8512877U1 (de) | 1985-05-02 | 1985-05-02 | Welle mit verstellbaren, ringförmigen Werkzeugen zur Vorbereitung von Wellpappe für deren Weiterverarbeitung für Maschinen zur Wellpappenherstellung |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP0201788A2 true EP0201788A2 (fr) | 1986-11-20 |
Family
ID=6780572
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP86105798A Withdrawn EP0201788A2 (fr) | 1985-05-02 | 1986-04-26 | Dispositif pour couper et/ou rainurer des bandes de papier |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0201788A2 (fr) |
| JP (1) | JPS6239194A (fr) |
| DE (1) | DE8512877U1 (fr) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0285697A3 (en) * | 1987-04-08 | 1989-12-20 | Elio Cavagna | Device for the selective or simultaneous traverse of the cutting members in a machine for the chopping and/or cutting of material in sheet |
| CN110039596A (zh) * | 2019-05-20 | 2019-07-23 | 深圳市凯思特医疗科技股份有限公司 | 一种切割刀套、切割刀具及切割装置 |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| SE524370C2 (sv) * | 2002-05-10 | 2004-08-03 | Tetra Laval Holdings & Finance | Förpackningslaminat, bigvals, samt ett skikt för användning till ett förpackningslaminat |
-
1985
- 1985-05-02 DE DE19858512877 patent/DE8512877U1/de not_active Expired
-
1986
- 1986-04-26 EP EP86105798A patent/EP0201788A2/fr not_active Withdrawn
- 1986-05-02 JP JP10120386A patent/JPS6239194A/ja active Pending
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0285697A3 (en) * | 1987-04-08 | 1989-12-20 | Elio Cavagna | Device for the selective or simultaneous traverse of the cutting members in a machine for the chopping and/or cutting of material in sheet |
| CN110039596A (zh) * | 2019-05-20 | 2019-07-23 | 深圳市凯思特医疗科技股份有限公司 | 一种切割刀套、切割刀具及切割装置 |
| CN110039596B (zh) * | 2019-05-20 | 2024-04-05 | 深圳市凯思特医疗科技股份有限公司 | 一种切割刀套、切割刀具及切割装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| DE8512877U1 (de) | 1985-06-13 |
| JPS6239194A (ja) | 1987-02-20 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE2011204C2 (de) | Vorrichtung zum Herstellen von Isolierstreifenabschnitten, die in Nuten eines Magnetkerns einsetzbar sind | |
| EP2181563B1 (fr) | Procédé de chauffage par induction | |
| DE3923525C2 (de) | Computertomographie-(CT)-Scanner | |
| CH643409A5 (de) | Vorrichtung zum wickeln von spulen fuer statoren elektrischer maschinen. | |
| DE2726321A1 (de) | Vorrichtung zum wickeln von rollen | |
| DE2313417C3 (de) | Vorrichtung zum Herstellen von verdrallten Leitungsdrahtpaaren und Verfahren zum Verdrallen von Leitungsdrahtpaaren | |
| DE4414003A1 (de) | Verfahren und Vorrichtung zum Aufwickeln von Warenbahnen, insbesondere Kunststoffolien in einer Mehrfach-Wendewickelmaschine | |
| DE2609957C3 (de) | Verfahren zum Zusammenbauen von unmagnetischen, elektrischleitenden Bauteilen | |
| EP0528115B1 (fr) | Dispositif pour former des bobines placées dans des paquets de tôles de stators ou rotors | |
| DE3390241T1 (de) | Vorrichtung zum Einführen von Keilen in die Nuten eines Magnetkerns | |
| EP3600713A1 (fr) | Dispositif, en particulier machine, pour la fabrication de fil de wiegand à partir d'un fil, en particulier d'un fil d'impulsion, et procédé pour le fonctionnement d'un dispositif | |
| DE69003834T2 (de) | Magnetische Walzvorrichtung. | |
| DE3535265C1 (de) | Schneid- und Rillvorrichtung fuer Papier- oder Pappebahnen | |
| EP0089006B1 (fr) | Machine de coupe | |
| DE1197969B (de) | Steuerschaltung fuer einen Antrieb mit wechselweise elektromagnetisch gesteuerter Antriebs- und Bremskupplung mit zwei bistabilen elektronischen Schaltern | |
| DE1427319A1 (de) | Verfahren und Einrichtung zur Herstellung von Magnetkernen | |
| DE102006028858A1 (de) | Transporteinrichtung | |
| AT238812B (de) | Verfahren und Vorrichtung zum wendelförmigen Wickeln eines Metallstreifens | |
| DE68911905T2 (de) | Elektrischer Motor ohne Stromwenderteile mit in der Richtung der Achse aufgestellten Polen und auf demselben Prinzip basierender magnetischer Motor. | |
| DD146878A5 (de) | Stanz-und wickelmaschine und mit ihr hergestellte elektrische geraete | |
| DE2917948C3 (de) | Hochgeschwindigkeitspresse | |
| DE202004011943U1 (de) | Vorrichtung zum Spannen von Werkzeugen | |
| DE2601463A1 (de) | Verfahren und vorrichtung zum entfernen der wicklungen von statoren elektrischer maschinen | |
| DE809929C (de) | Vielpunkt-Schweissmaschine | |
| DE3230460A1 (de) | Verfahren und vorrichtung zum speichern von energie |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH DE FR GB IT LI NL SE |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 19880503 |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: SCHULTZ, PETER Inventor name: SCHULTZ, KAETHE |