EP0224683A1 - Procédé de réglage de la tension du tissu sur une laineuse - Google Patents
Procédé de réglage de la tension du tissu sur une laineuse Download PDFInfo
- Publication number
- EP0224683A1 EP0224683A1 EP86114009A EP86114009A EP0224683A1 EP 0224683 A1 EP0224683 A1 EP 0224683A1 EP 86114009 A EP86114009 A EP 86114009A EP 86114009 A EP86114009 A EP 86114009A EP 0224683 A1 EP0224683 A1 EP 0224683A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- rollers
- tension
- roller
- rauhmaschine
- cloth
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000000034 method Methods 0.000 title claims abstract description 29
- 230000001105 regulatory effect Effects 0.000 title claims abstract description 6
- 239000004744 fabric Substances 0.000 claims abstract description 38
- 238000012544 monitoring process Methods 0.000 claims abstract description 4
- 239000011248 coating agent Substances 0.000 claims description 31
- 238000000576 coating method Methods 0.000 claims description 31
- 230000001419 dependent effect Effects 0.000 claims 1
- 239000013077 target material Substances 0.000 claims 1
- 238000005259 measurement Methods 0.000 abstract 1
- 238000012545 processing Methods 0.000 description 9
- 238000007788 roughening Methods 0.000 description 5
- 230000001680 brushing effect Effects 0.000 description 2
- 238000013461 design Methods 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 230000036316 preload Effects 0.000 description 2
- 230000006978 adaptation Effects 0.000 description 1
- 238000009530 blood pressure measurement Methods 0.000 description 1
- 238000005253 cladding Methods 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 239000000835 fiber Substances 0.000 description 1
- 238000007654 immersion Methods 0.000 description 1
- 238000012549 training Methods 0.000 description 1
Images



Classifications
-
- D—TEXTILES; PAPER
- D06—TREATMENT OF TEXTILES OR THE LIKE; LAUNDERING; FLEXIBLE MATERIALS NOT OTHERWISE PROVIDED FOR
- D06C—FINISHING, DRESSING, TENTERING OR STRETCHING TEXTILE FABRICS
- D06C11/00—Teasing, napping or otherwise roughening or raising pile of textile fabrics
Definitions
- the invention relates to a method for monitoring and / or regulating the fabric tension of fabric webs processed on a reel-nibbling machine, the napping machine having coating and / or counter-coating rollers on the jacket of the cylinder that act on the fabric with coating and / or counter-coating energy.
- the invention relates to a reel-up machine for carrying out the method according to the invention with coating and / or counter-coating rollers mounted on the jacket of the reel, a feed roller at the goods inlet and a take-off roller at the goods outlet.
- double-acting brushing machines are generally used, the brushing rollers arranged on the jacket of the reel as coating and counter-coating rollers with wire-cladding are trained.
- the wires of the line rollers generally point in the direction in which the goods travel over the reel, and the wires of the counter-line rollers point in the opposite direction.
- the goods are effectively roughened by an alternating arrangement of line and counter-roller, ie the fibers are lifted off the base of the fabric.
- a relaxation of the goods occurs between a line and a counter-roller and tension of the goods between a counter-line and a line roller.
- Optimal processing of goods on reel-to-reel machines therefore depends on the amount of line and counter-stroke energy as well as the overall tension on the reel. Even for trained and experienced specialists, it is difficult Always find the optimal processing parameters, especially if goods with different properties are to be processed one after the other.
- the invention is therefore based on the object of specifying a method with which the monitoring and / or regulation of the fabric tension can be automated in order to optimize the processing. Furthermore, a reel-up machine is to be specified for carrying out this method, in which the goods are automatically kept in the optimum tension in each case and are supplied with optimal stroke and / or counter-stroke energy, but which is nevertheless simple in construction and therefore economical.
- the method according to the invention is characterized in that for a specific product, a specific target voltage value at the goods inlet and at the goods outlet of the grooving machine, which ensures an optimal distribution of the goods tension on the drum, is set such that the goods tension is preferably measured continuously on the entry and exit sides during operation, checked and the voltage values are compared with each other, and that in the event of a deviation from the predetermined voltages, the respective deviating voltage is automatically reset to the predetermined target value.
- the invention is thus based on the knowledge that only from the comparison of the two product tension states before and after the reel, clear statements can be made about all the individual parameters that are important for processing, so that the respective deviating tension is preferably automatically set to the desired value by an electronic process computer can be.
- a reel-up machine for carrying out the method according to the invention is characterized in that a measuring device measuring the fabric tension is arranged at the goods inlet and at the goods outlet. These measuring devices are connected to an electronic process computer which compares the existing product tension conditions with one another and automatically sets the required compensation voltage on the basis of this comparison.
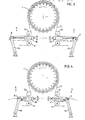
- a reel-up machine consists of a reel 1, the casing of which is formed in a manner known per se from conventional-type roughening rollers, namely from coating rollers S and counter-coating rollers G.
- the line rollers S and the counter-line rollers G apply a line and / or counter-line energy to a product 2 to be roughened, the course of which is shown by a chain line.
- a driven feed roller 4 is arranged at the goods inlet 3 and a likewise driven take-off roller 6 is arranged at the goods outlet 5.
- a measuring device measuring the tension of the goods is arranged according to the invention at the goods inlet 3 and at the goods outlet 5.
- the main elements of these measuring devices are two dancer rollers 7, 8 which are arranged between the feed roller 4 and the drum 1 on the one hand and between the drum 1 and the take-off roller 6 on the other hand.
- the dancer rollers 7, 8 are looped around by the goods 2.
- the dancer rollers 7, 8 are movable in a direction perpendicular to their axes of rotation and in the direction of the loops of the web 2 they form, in particular by means of pivot levers 13, 14. Two lateral pivot levers are provided for each dancer roller 7, 8.
- any change in the fabric tension is measured both at the goods inlet 3 and at the goods outlet 5 based on the position of the dancer rollers 7, 8, for which purpose each dancer roller 7, 8 is connected according to the invention to a linear actual value sensor 15, 16 that detects its position.
- These actual value transmitters 15, 16 can be, for example, conventional immersion potentiometers or similar measuring devices which convert a linear change in position into electrical output signals.
- the dancer rollers 7, 8 act against at least one pressure element 17, 18 that generates a preselectable preload. 2, two pressure elements 17 a, 17 b; 18 a, 18 b provided. In this way, a target product tension can be selected.
- the pressure elements 17, 18 are preferably designed as pneumatic piston-cylinder units, the amount of the preload being adjustable in the range from 0 to 300 N.
- the dancer rollers 7, 8 thus do not actively provide for a fabric tension, but act as passive measuring devices moved by the fabric by tension or relaxation.
- a separate drive in particular in each case a variable-speed DC motor 21, 22, 23, 24, 25, is provided for driving the drum 1, the line rollers S, the counter-coating rollers G, the feed roller 4 and the take-off roller 6.
- a separate drive in particular in each case a variable-speed DC motor 21, 22, 23, 24, 25, is provided for driving the drum 1, the line rollers S, the counter-coating rollers G, the feed roller 4 and the take-off roller 6.
- the linear actual value transmitters 15, 16, the pressure elements 17, 18 and the motors 21 to 25 are connected to an electronic process computer 26.
- An input device 27 is connected to the process computer 26 for inputting target values for adaptation to different materials.
- the electronic process computer 26 receives from the linear actual value transmitters 15, 16 electrical actual value signals which are proportional to the product tension present in each case.
- the computer 26 compares these values and uses them to calculate the voltage compensation required in each case, which is subsequently set by optimally adjusting the speed of all the individual drives.
- Fig. 3 it is shown that the fabric tension at both the goods inlet 3 and the goods outlet 5 is too low, so that both dancer rollers 7, 8 due to the prestressed pressure elements 17, 18 have extended the goods loop.
- the positions of the dancer rollers 7, 8 shown are passed on to the process computer by the linear actual value transmitters (not shown). This is programmed so that in this case it increases the speed of the take-off roller 6, whereby the goods as a whole are stretched.
- Fig. 5 shows a state in which the coating energy is too high in relation to the counter-coating energy, since the goods 2 are transported too strongly by the drum 1, so that the goods are stretched at the goods inlet 3 by the high tension of the drum 1 and at the goods outlet 5 is relaxed.
- the computer causes a reduction in the stroke energy, i.e. a speed reduction of the drive motor 22 of the line rollers S.
- the invention is in no way limited to the exemplary embodiment shown. So it is entirely within the scope of the invention to measure the tension of the web with equivalent means, such as. B. with strain gauges, hydraulic or pneumatic pressure measurements or the like.
- the dancer rollers 7, 8 can also be linear, ie without a pivot lever, be movably stored. It is also possible to dispense entirely with dancer rollers and to measure the fabric tension only by suitable means, for example pressure gauges, in the deflection rollers 11, 12.
- suitable means for example pressure gauges, in the deflection rollers 11, 12.
- the training with the dancer rollers 7, 8 has the advantage that a pretension can be adjusted to adapt to different materials to be processed.
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Treatment Of Fiber Materials (AREA)
- Controlling Rewinding, Feeding, Winding, Or Abnormalities Of Webs (AREA)
- Preliminary Treatment Of Fibers (AREA)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT86114009T ATE74385T1 (de) | 1985-11-16 | 1986-10-09 | Verfahren zur regelung der warenspannung bei tambour-rauhmaschinen sowie tambour-rauhmaschine. |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3540689 | 1985-11-16 | ||
| DE19853540689 DE3540689A1 (de) | 1985-11-16 | 1985-11-16 | Verfahren zur regelung der warenspannung bei tambour-rauhmaschinen sowie tambour-rauhmaschine |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0224683A1 true EP0224683A1 (fr) | 1987-06-10 |
| EP0224683B1 EP0224683B1 (fr) | 1992-04-01 |
Family
ID=6286160
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP86114009A Expired - Lifetime EP0224683B1 (fr) | 1985-11-16 | 1986-10-09 | Procédé de réglage de la tension du tissu sur une laineuse |
Country Status (5)
| Country | Link |
|---|---|
| US (1) | US4803761A (fr) |
| EP (1) | EP0224683B1 (fr) |
| AT (1) | ATE74385T1 (fr) |
| DE (2) | DE3540689A1 (fr) |
| ES (1) | ES2030655T3 (fr) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0613972A1 (fr) * | 1993-03-04 | 1994-09-07 | MARIO CROSTA S.r.l. | Dispositif de protection des coutures pour machine d'abrasion ou de lainage à tambour |
| EP0649927A3 (fr) * | 1993-08-30 | 1996-02-14 | Sperotto Rimar Spa | Laineuse pour tissu ou tricot avec contrÔle de tension. |
Families Citing this family (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE8707501U1 (de) * | 1987-05-25 | 1987-08-27 | Rommerskirchen, Matthias, 4150 Krefeld | Tambour-Rauhmaschine mit Vorrichtung zum Rauhen von Textilwaren |
| DE3731898A1 (de) * | 1987-09-23 | 1989-04-13 | Sucker & Franz Mueller Gmbh | Verfahren zum regeln des rauhprozesses auf einer kratzenrauhmaschine und vorrichtung zum durchfuehren des verfahrens |
| US5084948A (en) * | 1990-06-18 | 1992-02-04 | Guilford Mills, Inc. | Textile napping machine |
| US6058582A (en) * | 1997-10-03 | 2000-05-09 | Parks & Woolson | Napper machine |
| IT1295663B1 (it) * | 1997-10-08 | 1999-05-24 | Tintoria Rifinizione Nuove Ide | Macchina garzatrice comprendente un sistema di regolazione della traiettoria del tessuto in trattamento |
| US6141842A (en) * | 1999-05-21 | 2000-11-07 | Parks & Woolson Machine Company | Dynamic zoning assembly in a napper machine |
| US6325322B1 (en) | 1999-10-06 | 2001-12-04 | Presstek, Inc. | Dual-plate winding mechanism with tension adjustment |
| ITFI20010237A1 (it) * | 2001-12-14 | 2003-06-16 | Coramtex Srl | Macchina per il trattamento di tessuti e relativo metodo |
| US20070154678A1 (en) * | 2002-07-15 | 2007-07-05 | Emery Nathan B | Napped fabric and process |
| ITFI20030215A1 (it) * | 2003-08-06 | 2005-02-07 | Coramtex Srl | Macchina perfezionata per il trattamento dei tessuti. |
| CN104555536A (zh) * | 2015-01-16 | 2015-04-29 | 苏州经贸职业技术学院 | 一种织物张力控制装置 |
| CN105063947B (zh) * | 2015-08-07 | 2018-02-27 | 浙江彩蝶实业有限公司 | 一种布料双面起毛机 |
| ITUB20154285A1 (it) * | 2015-10-09 | 2017-04-09 | Lafer Spa | Macchina per il trattamento di prodotti tessili |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB907658A (en) * | 1958-04-01 | 1962-10-10 | Cotton Silk & Man Made Fibres | Improvements in or relating to textile raising machines |
| FR1522222A (fr) * | 1964-06-04 | 1968-04-26 | Tomlinsons Rochdale Ltd | Procédé et machine à gratter ou lainer à chardons métalliques |
| DE1760830A1 (de) * | 1968-07-06 | 1972-01-05 | Mueller Franz | Tambour-Rauhmaschine |
| FR2573101A1 (fr) * | 1984-11-09 | 1986-05-16 | Mach Textiles | Procede de regulation automatique des parametres de travail d'une laineuse et laineuse automatisee a l'aide de ce procede |
Family Cites Families (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB796729A (en) * | 1953-10-19 | 1958-06-18 | Caspar Monforts Von Hobe | Improvements in and relating to fabric raising machines |
| DE1106723B (de) * | 1953-10-19 | 1961-05-18 | Monforts Fa A | Rauhmaschine |
| US2923046A (en) * | 1955-06-23 | 1960-02-02 | Albert C Scholaert | Automatic device for adjusting the tension of the fabric in finishing machines |
| DE1078529B (de) * | 1955-06-23 | 1960-03-31 | A C Scholaert Ets | Verfahren und Vorrichtung zum Rauhen von Textilstoffbahnen |
| NL6409767A (fr) * | 1963-11-07 | 1965-05-10 | ||
| US3857023A (en) * | 1973-06-21 | 1974-12-24 | Industrial Nucleonics Corp | Method and apparatus for improving the uniformity of the basic weight of a fabric |
| FR2338343A1 (fr) * | 1976-01-16 | 1977-08-12 | Scholaert Michel | Perfectionnement aux laineuses a travailleurs poil et travailleurs contrepoil |
| DE3213716A1 (de) * | 1982-04-14 | 1983-10-20 | A. Monforts GmbH & Co, 4050 Mönchengladbach | Gummiband-krumpfanlage |
-
1985
- 1985-11-16 DE DE19853540689 patent/DE3540689A1/de active Granted
-
1986
- 1986-10-09 ES ES198686114009T patent/ES2030655T3/es not_active Expired - Lifetime
- 1986-10-09 EP EP86114009A patent/EP0224683B1/fr not_active Expired - Lifetime
- 1986-10-09 AT AT86114009T patent/ATE74385T1/de active
- 1986-10-09 DE DE8686114009T patent/DE3684672D1/de not_active Expired - Lifetime
- 1986-11-06 US US06/927,763 patent/US4803761A/en not_active Expired - Fee Related
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB907658A (en) * | 1958-04-01 | 1962-10-10 | Cotton Silk & Man Made Fibres | Improvements in or relating to textile raising machines |
| FR1522222A (fr) * | 1964-06-04 | 1968-04-26 | Tomlinsons Rochdale Ltd | Procédé et machine à gratter ou lainer à chardons métalliques |
| DE1760830A1 (de) * | 1968-07-06 | 1972-01-05 | Mueller Franz | Tambour-Rauhmaschine |
| FR2573101A1 (fr) * | 1984-11-09 | 1986-05-16 | Mach Textiles | Procede de regulation automatique des parametres de travail d'une laineuse et laineuse automatisee a l'aide de ce procede |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0613972A1 (fr) * | 1993-03-04 | 1994-09-07 | MARIO CROSTA S.r.l. | Dispositif de protection des coutures pour machine d'abrasion ou de lainage à tambour |
| EP0649927A3 (fr) * | 1993-08-30 | 1996-02-14 | Sperotto Rimar Spa | Laineuse pour tissu ou tricot avec contrÔle de tension. |
Also Published As
| Publication number | Publication date |
|---|---|
| DE3540689C2 (fr) | 1988-01-07 |
| DE3684672D1 (de) | 1992-05-07 |
| ES2030655T3 (es) | 1992-11-16 |
| EP0224683B1 (fr) | 1992-04-01 |
| ATE74385T1 (de) | 1992-04-15 |
| DE3540689A1 (de) | 1987-05-21 |
| US4803761A (en) | 1989-02-14 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0224683B1 (fr) | Procédé de réglage de la tension du tissu sur une laineuse | |
| DE68926199T2 (de) | Streckvorrichtung mit selbsttätigem Ausgleich | |
| EP0275471A1 (fr) | Procédé et appareil pour égaliser la densité d'un voile de fibres à l'entrée d'une machine textile | |
| EP0036002B1 (fr) | Dispositif de commande de la vitesse de rotation des broches d'un banc a broches | |
| EP2034059B1 (fr) | Procédé de détermination du poids lineaire d'un ruban de fibres et machine de préparation de filature | |
| CH708290A2 (de) | Wickelmaschine und Verfahren zum Wickeln von Watte aus Faserbändern. | |
| DE1427888A1 (de) | Verfahren und Vorrichtung zur Beeinflussung der Dicke von gewalztem Bandmaterial | |
| WO1998024969A1 (fr) | Calandre | |
| DE10004604B4 (de) | Vorrichtung zum Zuführen von Faserbändern an einer Spinnereimaschine, insbesondere Strecke, z.B. Regulierstrecke | |
| CH661754A5 (de) | Regeleinrichtung fuer den drehantrieb einer abwickelvorrichtung. | |
| DE10140645B4 (de) | Verfahren zum Betreiben eines Streckwerks sowie Streckwerk | |
| DE2812100C2 (de) | Verfahren zum Führen eines aus Einzelsträngen zusammengesetzten Gesamtstranges und Herstellen von gefachten Drahtspulen sowie Vorrichtung zum Durchführen des Verfahrens | |
| EP1573110B1 (fr) | Dispositif pour appreter des tissus denim | |
| EP0307558A2 (fr) | Installation de traitement d'une matière sans fin | |
| CH696121A5 (de) | Vorrichtung an einem Streckwerk für Faserbänder, z.B. einer Strecke, zum Ermitteln von Einstellwerten für den Vorverzug. | |
| DE3510521A1 (de) | Verfahren zum einstellen der betriebsparameter einer spinnmaschine | |
| DE19810108A1 (de) | Maschine zum Bilden von Wattewickeln | |
| DE3932385A1 (de) | Textilmaschine, insbesondere kettfadenwickelmaschine | |
| AT396125B (de) | Vorrichtung zum aufbringen eines vliesbandes auf eine endlos umlaufende traegerbahn | |
| DE4323715C1 (de) | Verfahren zum Kompressivkrumpfen und Kompressivkrumpfanlage | |
| DE9112257U1 (de) | Konusschärmaschine | |
| DE3884260T2 (de) | Steuerung von Karden. | |
| EP0891435B1 (fr) | Dispositif pour mesurer l'epaisseur et/ou l'inegalite d'ouates ou de non-tisses | |
| EP0503308A2 (fr) | Procédé et appareil pour convertir, notamment par découpage de câbles de fibres chimiques en rubans de fibres filables | |
| CH696666A8 (de) | Vorrichtung zum Dublieren und Verziehen von Faserbaendern. |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE ES FR GB GR IT LI LU NL SE |
|
| 17P | Request for examination filed |
Effective date: 19870526 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: JOHANNES MENSCHNER MASCHINENFABRIK GMBH & CO KG |
|
| 17Q | First examination report despatched |
Effective date: 19900502 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE ES FR GB GR IT LI LU NL SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19920401 Ref country code: NL Effective date: 19920401 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19920401 Ref country code: BE Effective date: 19920401 |
|
| REF | Corresponds to: |
Ref document number: 74385 Country of ref document: AT Date of ref document: 19920415 Kind code of ref document: T |
|
| ET | Fr: translation filed | ||
| REF | Corresponds to: |
Ref document number: 3684672 Country of ref document: DE Date of ref document: 19920507 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| ITF | It: translation for a ep patent filed | ||
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19920925 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19920928 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Effective date: 19921009 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19921009 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 19921013 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 19921016 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19921031 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2030655 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19931009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 19931011 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19931031 Ref country code: CH Effective date: 19931031 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19931009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19940630 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19940701 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 19990601 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20051009 |