EP0244265B1 - Druckanhaftende Etiketten in Stapelform - Google Patents
Druckanhaftende Etiketten in Stapelform Download PDFInfo
- Publication number
- EP0244265B1 EP0244265B1 EP19870303937 EP87303937A EP0244265B1 EP 0244265 B1 EP0244265 B1 EP 0244265B1 EP 19870303937 EP19870303937 EP 19870303937 EP 87303937 A EP87303937 A EP 87303937A EP 0244265 B1 EP0244265 B1 EP 0244265B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- labels
- label
- block
- articles
- release coating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired
Links
- 238000000576 coating method Methods 0.000 claims description 40
- 239000011248 coating agent Substances 0.000 claims description 36
- 238000000034 method Methods 0.000 claims description 16
- 239000000853 adhesive Substances 0.000 claims description 15
- 230000001070 adhesive effect Effects 0.000 claims description 15
- 239000004820 Pressure-sensitive adhesive Substances 0.000 claims description 10
- 239000012790 adhesive layer Substances 0.000 claims description 9
- 230000002093 peripheral effect Effects 0.000 claims description 5
- 238000004519 manufacturing process Methods 0.000 claims description 4
- 238000005096 rolling process Methods 0.000 claims description 2
- 238000002372 labelling Methods 0.000 description 6
- 239000010410 layer Substances 0.000 description 5
- 238000005520 cutting process Methods 0.000 description 3
- 239000000463 material Substances 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000002699 waste material Substances 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B31—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER; WORKING PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER
- B31D—MAKING ARTICLES OF PAPER, CARDBOARD OR MATERIAL WORKED IN A MANNER ANALOGOUS TO PAPER, NOT PROVIDED FOR IN SUBCLASSES B31B OR B31C
- B31D1/00—Multiple-step processes for making flat articles ; Making flat articles
- B31D1/02—Multiple-step processes for making flat articles ; Making flat articles the articles being labels or tags
- B31D1/026—Cutting or perforating
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65C—LABELLING OR TAGGING MACHINES, APPARATUS, OR PROCESSES
- B65C3/00—Labelling other than flat surfaces
- B65C3/06—Affixing labels to short rigid containers
- B65C3/08—Affixing labels to short rigid containers to container bodies
- B65C3/14—Affixing labels to short rigid containers to container bodies the container being positioned for labelling with its centre-line vertical
- B65C3/16—Affixing labels to short rigid containers to container bodies the container being positioned for labelling with its centre-line vertical by rolling the labels onto cylindrical containers, e.g. bottles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65C—LABELLING OR TAGGING MACHINES, APPARATUS, OR PROCESSES
- B65C9/00—Details of labelling machines or apparatus
- B65C9/08—Label feeding
- B65C9/12—Removing separate labels from stacks
- B65C9/14—Removing separate labels from stacks by vacuum
Definitions
- This invention is concerned with labels for application to products generally but especially to cans and bottles.
- Labels have previously been proposed that have a pressure sensitive adhesive layer on one side thereof, the layer being protected, prior to application of the label to a product, by a backing sheet. Such labels have proved popular despite the complication and waste inherent in the use of the backing sheet.
- a method of making a block of labels from a continuous label stock having a front face on which the labels are printed, a release coating on the front face and a pressure sensitive adhesive coating on the rear face thereof comprising using a hollow die to cut labels in succession from the label stock such that each label when cut enters the die and pushes previously cut labels further into the die, and removing from the die the block of superimposed labels, adjacent labels having an adhesive coating contacting a release coating.
- the present invention further provides a method of applying to articles of circular cross-section labels from a block (22) of labels comprising superimposed labels each having a pressure sensitive adhesive coating (17) on the back face thereof and a release coating (16) on the front face thereof, the adhesive coating overlying the release coating of the adjacent label, the method comprising locating the block (22) of labels to project laterally into a line of articles (30) for engagement with the peripheral surfaces of the articles, the adhesive surface (17) of the end label adjacent the line being exposed, and rolling the articles past the block of labels so that each article engages the exposed adhesive layer of the end label and peels that label off the block to expose the adhesive layer of the next label to the next article.
- the present invention additionally provides apparatus for applying to articles (30) of circular cross-section labels from a block (22) of labels comprising superimposed labels each having a pressure sensitive adhesive coating (17) on the back face thereof and a release coating (16) on the front face thereof, the adhesive coating overlying the release coating of the adjacent label, the apparatus comprising a guide (32) spaced from one flight (37) of a continuous belt (36) to define therewith a feed path in which the articles are engaged between the guide and the belt, means (39) for driving the flight of the belt in a feed direction to roll the articles along the guide, and a label holder (38) for feeding the block (22) of labels laterally into the feed path so that the adhesive coatings on the labels are presented in succession to the peripheral surfaces of successive articles as they pass the label holder.
- a further method of applying labels is provided as specified in claim 5.
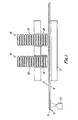
- Fig. 1 diagrammatically illustrates the formation of blocks of label 10 from a continuous label stock (12).
- the continuous stock (12) may be performed by a series of conventional, in-line operations in which the label base material is firstly printed with the label design on its front face, and then presented for the application thereto of a release coating on its front face and a pressure sensitive adhesive coating to its rear face, the application of the coatings being associated with respective curing operations if necessary.
- the precise method by which the continuous stock 12 is produced may be varied, but essen- tally the stock 12, when it reaches the last process stage illustrated in Fig. 1, comprises a base 15 on which the labels are printed and having a release coating 16 on its front face and a pressure sensi- five adhesive coating 17 on its rear face. While the stock is. shown face down in Fig. 1, it could equally well be face up.
- the continuous stock 12 is passed to a die cutting station in which a number, in this embodiment two, of hollow dies 20 are actuated to co-operate with a cutting base 21 to cut the printed labels from the stock 12, operation of the dies being registered with the position of the labels by suitable means, in this embodiment a light scanning device 23 viewing the labels on the incoming stock 12.
- each label As each label is cut by a die 20, it enters the die and pushes further into the die the label previously cut by the die so that a stack 22 of labels is built up in the die.
- the adhesive coating 17 on the rear face of each label adheres slightly to the release coating 16 on the front face of the previously cut label, the stack 22 of labels can be removed from the die as a unitary block which greatly facilitates subsequent handling and is advantageous in simplifying the subsequent application of the labels to the appropriate goods as it dispenses with the unrolling, cutting, and individual label handling operations associated with the application of labels from reels. It may be desirable to protect the exposed adhesive layer at the end of the stack by means of a release liner during handling and transport.
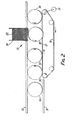
- Fig. 2 there is illustrated one method of applying to containers of circular cross-section, such as cans or bottles, labels from a block 22 of labels.
- the containers 30, seen in Fig. 2 in plan view, are fed towards the labelling station 35 between guide rails 31 and 32, one guide rail 31 being replaced in the vicinity of the station 35 by a continuous rubber belt 36 entrained round drive/pulley wheels or rollers and which is driven so that its inner flight 37, which engages the containers 30, is moving in the direction of feed.
- the belt 36 is driven by a motor 39.
- the spacing between the inner flight 37 of the belt 36 and the guide rail 32 is such that the containers 30 are trapped between the belt and the rail and are thus forced to roll on the guide rail 32 past the labelling station 35.
- a label holder or magazine comprising a hollow guide 38 in which a label block 22 is downwardly biased.
- the guide supports the block 22 so that it projects laterally into the feed path and exposes the adhesive layer on the first label to the periphery of the next container.
- the block 22 is inverted so that it is the release coating of each label that is in turn exposed at the end of the guide 38.
- a fixed vacuum roller beneath the guide 38 peels the labels in succession from the block and deposits them, adhesive side down, on articles passing the roller on the other side of the roller from the guide 38, the velocity of the articles passing the roller matching the peripheral velocity of the roller as it contacts the articles.
- the belt 36 could be made of a material other than rubber provided only that it is biased into engagement with the containers 30.
Landscapes
- Labeling Devices (AREA)
- Making Paper Articles (AREA)
Claims (5)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| GB8610660 | 1986-05-01 | ||
| GB8610660A GB2189768B (en) | 1986-05-01 | 1986-05-01 | Pressure sensitive labels in block form |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0244265A1 EP0244265A1 (de) | 1987-11-04 |
| EP0244265B1 true EP0244265B1 (de) | 1990-04-25 |
Family
ID=10597169
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19870303937 Expired EP0244265B1 (de) | 1986-05-01 | 1987-05-01 | Druckanhaftende Etiketten in Stapelform |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0244265B1 (de) |
| DE (1) | DE3762405D1 (de) |
| GB (1) | GB2189768B (de) |
Families Citing this family (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2224691A (en) * | 1988-09-21 | 1990-05-16 | Fkb Group Plc | Coupon |
| CA2017893A1 (en) * | 1989-06-02 | 1990-12-02 | Seinosuke Horiki | Method for a surface treatment |
| CA2017892A1 (en) * | 1989-06-02 | 1990-12-02 | Nagoya Oilchemical Co., Ltd. | Accumulation of masking members and an attaching method thereof |
| JPH033479U (de) * | 1989-06-02 | 1991-01-14 | ||
| JPH0728935Y2 (ja) * | 1989-06-02 | 1995-07-05 | 名古屋油化株式会社 | マスキング材の取付装置 |
| ITVI980185A1 (it) * | 1998-09-29 | 2000-03-29 | Antonio Riglietti | Macchina fustellatrice |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| BE498579A (de) * | ||||
| US3145514A (en) * | 1962-07-06 | 1964-08-25 | Edmond A Steffey | Method for packaging appliques |
| DE1586358A1 (de) * | 1967-01-27 | 1970-04-23 | Mario Ciliotta | Automatische Flaschenetikettiermaschine mit einem einzigen,ununterbrochen in der gleichen Richtung rotierenden Mehrfachspeicherbehaelter |
| DE2003279A1 (de) * | 1970-01-26 | 1971-08-05 | Ploss U | Maschine zum Aufbringen einer Dekoration auf Hohlkoerper aus Kunststoff,beispielsweise Flaschen |
| DE2225586A1 (de) * | 1972-05-26 | 1973-12-06 | Jacob Geb Lorbeer Hannelore | Automatisch arbeitende einrichtung zum schneiden, stanzen, buendeln und verpacken von etiketten und aehnlichen blattschnitten |
| GB1470274A (en) * | 1975-04-01 | 1977-04-14 | Seton Name Plate Corp | Stamped information tags |
| US4097627A (en) * | 1976-11-22 | 1978-06-27 | Avery International Corporation | Double faced tab fastener characterized by a strip of release agent designed to extend partly beyond the width of a strip of adhesive |
| NL7900190A (nl) * | 1978-01-16 | 1979-07-18 | Cosco Ind | Etiket. |
| US4416392A (en) * | 1981-02-19 | 1983-11-22 | Minnesota Mining & Manufacturing Company | Dispenser for adhesive coated sheet material |
| US4501772A (en) * | 1984-03-15 | 1985-02-26 | Luxeder William P | Process for producing ultra removable pressure sensitive labels |
| JPS6169534A (ja) * | 1984-09-11 | 1986-04-10 | 株式会社 サト− | ラベル自動貼付機 |
| US4565596A (en) * | 1984-11-20 | 1986-01-21 | Clowe Henry W | Tapered container labeling apparatus and method |
-
1986
- 1986-05-01 GB GB8610660A patent/GB2189768B/en not_active Expired - Lifetime
-
1987
- 1987-05-01 EP EP19870303937 patent/EP0244265B1/de not_active Expired
- 1987-05-01 DE DE8787303937T patent/DE3762405D1/de not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| GB8610660D0 (en) | 1986-06-04 |
| GB2189768B (en) | 1990-07-11 |
| GB2189768A (en) | 1987-11-04 |
| EP0244265A1 (de) | 1987-11-04 |
| DE3762405D1 (de) | 1990-05-31 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| AU618047B2 (en) | Method of producing blocks of self-adhesive labels or the like and of applying the labels to a body | |
| US5674345A (en) | Linerless label printer applicator | |
| US3865671A (en) | Labeling device for upright standing objects | |
| US4475969A (en) | Label roll manufacture | |
| EP0275670B1 (de) | Verfahren und Apparat zum Verfertigen von Etiketten | |
| US6431241B1 (en) | Roll-fed labelling apparatus | |
| US4549454A (en) | Method for cutting and supplying labels of various shapes | |
| EP0794917B1 (de) | Konstruktion nicht-quadratischer trägerbahnloser etiketten, verfahren zum verwenden und zum aufbringen derselben, sowie entsprechende vorrichtung | |
| US6187128B1 (en) | Apparatus and method for converting and applying labels | |
| US20010023895A1 (en) | Debit card having secure scratch-off label strip and method of applying same | |
| HK1041858A1 (en) | Labeling apparatus and method | |
| US6841018B2 (en) | Label reconciliation device and method | |
| US3553049A (en) | Method of and apparatus for applying labels to bottles | |
| EP0244265A1 (de) | Druckanhaftende Etiketten in Stapelform | |
| WO2008010868A1 (en) | Method and device for high speed labeling of articles using two-sided labelstock | |
| EP0377384B1 (de) | Vorrichtung und Verfahren zum schnellen und genauen Etikettieren | |
| JPH09500856A (ja) | 包装容器のラベル貼り方法とラベル貼り装置 | |
| JP2002520231A (ja) | 積層体からのシート状製品の製造、それらのカバーフィルムへの移送および仕上げを行う方法と装置 | |
| US4119482A (en) | Apparatus for selectively printing and applying labels to articles of different sizes and shapes | |
| US5340430A (en) | System for handling a waste web of a web laminate | |
| GB2328427A (en) | Labelling with labels cut from non-backed strip | |
| EP1055604A1 (de) | Vorrichtung und Verfahren zum Ausschneiden von Etiketten aus einer auf einer Basisfolie haftende Etikettenfolie und zum Anbringen dieser Etiketten | |
| WO2001002253A1 (en) | A method and an apparatus for affixation of labels | |
| US20050087307A1 (en) | Application device for labels that vary in length | |
| US4132053A (en) | Apparatus for securing articles to a display board |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE FR NL |
|
| 17P | Request for examination filed |
Effective date: 19880504 |
|
| 17Q | First examination report despatched |
Effective date: 19890529 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR NL |
|
| REF | Corresponds to: |
Ref document number: 3762405 Country of ref document: DE Date of ref document: 19900531 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 19930531 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19941201 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19970421 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19970428 Year of fee payment: 11 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990302 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |