EP0366980A2 - Method and apparatus for continuous treatment of textile webs - Google Patents
Method and apparatus for continuous treatment of textile webs Download PDFInfo
- Publication number
- EP0366980A2 EP0366980A2 EP89118743A EP89118743A EP0366980A2 EP 0366980 A2 EP0366980 A2 EP 0366980A2 EP 89118743 A EP89118743 A EP 89118743A EP 89118743 A EP89118743 A EP 89118743A EP 0366980 A2 EP0366980 A2 EP 0366980A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- laying
- textile
- conveyor belt
- stacks
- textile web
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H45/00—Folding thin material
- B65H45/02—Folding limp material without application of pressure to define or form crease lines
- B65H45/06—Folding webs
- B65H45/10—Folding webs transversely
- B65H45/101—Folding webs transversely in combination with laying, i.e. forming a zig-zag pile
- B65H45/103—Folding webs transversely in combination with laying, i.e. forming a zig-zag pile by a carriage which reciprocates above the laying station
- B65H45/105—Folding webs transversely in combination with laying, i.e. forming a zig-zag pile by a carriage which reciprocates above the laying station coacting with fold holders
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/40—Type of handling process
- B65H2301/42—Piling, depiling, handling piles
- B65H2301/421—Forming a pile
- B65H2301/4216—Forming a pile of web folded in zig-zag form
- B65H2301/42162—Juxtaposing several piles
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2701/00—Handled material; Storage means
- B65H2701/10—Handled articles or webs
- B65H2701/18—Form of handled article or web
- B65H2701/182—Piled package
- B65H2701/1824—Web material folded in zig-zag form
- B65H2701/18242—Juxtaposed sets
Definitions
- Sheets of textile fabric, knitting and of textile-like material, such as are known under the term "non-woven", are placed in a stack of folds after completion of their substantial completion by means of a laying device and are fed in this form for further processing.
- the textile webs produced in this way also have a limited length. Therefore, the primarily thermal treatment cycles, but also chemical treatment processes can only be carried out for short periods, or the system must be shut down in order to be able to introduce a new textile web. In this way, not only is the processing time extended and the manufacturing costs increased, but uncontrolledly long exposure to processing media can sometimes lead to considerable quality reductions, often to rejects.
- the invention is based on the method defined at the outset and pursues the task of developing this method in such a way that the implementation or reintroduction of textile webs is largely avoided during the functional period of a process engineering treatment.
- the short textile webs can be separated from one another immediately after the individual fold stacks have been completed, but there is no need for this, i.e. the stack of folds still connected can be conveyed further and optionally subjected to a further continuous or step-wise treatment.
- contactlessly scannable signal elements are incorporated on or with a fixed assignment to the connection points between adjacent short paths, the presence of which is sensed at a predetermined passage point of the long textile path and used for control purposes for laying the textile path and further conveying the fold stacks thus formed.
- the control impulses generally originate from the textile web to be processed, in particular from the area of the connection points between adjacent short webs. It is desirable, but not necessary, that these short paths have the same length and that the signal elements are always assigned to the connection point in a certain way.
- the distance between the touch point for the signal element and the laying device should be measured and matched to a large number of pleat widths or laying lengths.
- connection point with the signal element has reached so far beyond the laying area that it comes to lie at a distance between two adjacent fold stacks.
- the web can then be cut as required in order to supply the individual, otherwise undamaged, short webs to different further treatments.
- the invention further relates to a device for folding and laying textile webs in stacks, wherein a plurality of shorter textile webs are connected at their ends to form a single long textile web, and then the long textile web is folded with units of the shorter textile webs and placed in stacks, in particular, in a continuous pass
- a detector for scanning a signal element incorporated in at least one connecting point or with a specific assignment to a connecting point in the textile web for controlling a laying device for forming individual fold stacks and their removal in Assignment to adjacent fold stacks is appropriate.
- the controller triggered by the detector can have a program memory with a selection device for preselecting a work program in accordance with the nature, dimensions and treatment of the respective textile web and the distance of the transport path between the detector and the laying device.
- a mostly tubular textile web (2) is drawn off from a feed store (1) and fed through a steaming calender (3) with calender rollers (4) to a cooling zone (5) and then to a laying device (6), the individual pleat stacks ( 7) forms, which are conveyed at intervals between a roller conveyor (8).
- the (long) textile web (2) is composed of individual short textile webs (21, 22, 23, 24, etc.).
- the laying device (6) has a height-adjustable laying carriage (11) with guide rollers (12) and bow rollers (13), and a laying table (14) with a conveyor belt (15) guided over it.
- the laying table (14) can be moved back and forth between the forward position drawn with full lines and the backward position (16) drawn in with the dash-dot lines and thereby covers a laying stroke h corresponding to the length of the folds.
- This laying table (14) is connected to an endless chain, which is tensioned between two deflection rollers parallel to the table guide and carries an engagement part such as a sliding block, which extends into a sliding guide provided on the laying slide (11) and runs transversely to the slide guide takes hold.
- the drive of the conveyor belt (15), not shown, is controlled on the one hand by a table limit switch (18) attached to the machine frame, which is actuated by the stop (20) attached to the laying table (14), and on the other hand by means of a attached to the laying table (14)
- Cam switch (28) by means of cams (29) provided on the conveyor belt (15) at intervals of the laying stroke (h).
- the removal conveyor belt (30) upstream of the roller conveyor is arranged in a frame-fixed manner, which is switched on and set in motion for the removal operation via the table limit switch (17) attached to the machine frame, by means of the stop (19) attached to the laying table (14) and via an on the laying table (14) attached cam switch (28) is brought to a standstill by cams (29) provided at intervals of the laying stroke h on the conveyor belt (15).
- connection points (37) are firmly connected to one another in the connection points (37), in particular sewn transversely to the web direction.
- a signal element (32), indicated here by a thickening of the web, is incorporated in the seam or at least close to the connection point, for example a metallic thread. Since the textile web (2) passes close to a detector (33), for example a UV detector, the latter always sends a trigger signal to the controller (34).
- the guide length between the detector (33) and a point in the area of the laying device must correspond to a whole multiple of the fold length or the laying stroke (h). As a rule, a single measurement is sufficient, but adjustment means can also be provided to adapt the actual guide length to the laying stroke.
- this distance corresponds to approximately half the length of the short textile web (22), and the second signal transmitter (321) hangs in a web loop (36) between the two fold stacks (7) and (71), the preceding one Signal generator (322) between the fold stacks (71) and (72).
- connection point (37) with the signal element (32) has approached the stack (7) according to FIG. 3 to one or two fold lengths h, a sequential circuit is triggered when the rear table switch (17) is actuated, and the conveyor belt ( 30) set in motion at the same speed as the laying table (14). If, according to FIG. 5, the front table switch (18) is still actuated in a connection position to the conveyor belt (30), the laying table (14) remains in this right end position.
- the conveyor belt (15) on the laying table (14) is set in motion at the same speed as the conveyor belt (30), the cam (29) running off the belt switch (28), the stack of folds (7) on the conveyor belt ( 30) transferred and the stack (71) is pushed from the conveyor belt onto the roller conveyor (8) and pushes the stack (72) onward.
- the conveyor belt (30) comes to a standstill and the laying carriage (11) moves to its lower starting position.
- the conveyor belt (15) runs one layer length to form the loop (36). If the belt switch (28) is actuated by the next cam, the conveyor belt (15) stops and the laying table (14) begins to move back and forth.
- the signal element can be self-radiation active, but the property of tactility by any of the known detectors is sufficient.
- the program memory (not shown) can be combined with other control units in the controller (34), which receives its trigger pulse from the detector (33).
- the program selector must also experience every similar training and arrangement.
Landscapes
- Treatment Of Fiber Materials (AREA)
Abstract
Um die verfahrenstechnische Behandlung von Textilstoff wie Gewebe oder Strickwerk und auch textilartigem Werkstoff zu vereinfachen, werden einzelne kurze Textilbahnen (21-24) an ihren Bahnenden (31) zu einer einzigen langen Textilbahn (2) verbunden und einer verfahrenstechnischen Behandlung in kontinuierlichem Durchlauf unterworfen, dann in Einheiten der kürzeren Textilbahnen gefaltet und lose verbunden in Teilstapeln (7, 71,72,...) abgelegt. Die lange Textilbahn (2) kann unverzüglich oder nach einer Zwischenlagerung als Ganzes einer weiteren kontinuierlichen Behandlung unterzogen und nach Bedarf wieder unterteilt werden. Auf diese Weise wird der Aufwand für Umsetzen oder Neueinführung bei Textilbahnen (21-24) während der Funktionsdauer einer bestimmten verfahrenstechnischen Behandlung weitgehend vermieden. Erleichtert werden kann die Ausführung des Verfahrens durch eine Vorrichtung zum Falten und Legen, wobei dicht an der Textilbahn (21-24) mit vorgegebenem Abstand von der Legevorrichtung (6) ein Detektor (33) vorgesehen ist, der die Verbindungsstellen (37) oder mit bestimmtem Abstand von diesen in die Textilbahn (21-24) eingearbeiteten Signalelemente (32) ertastet und danach die Bildung von Faltenstapeln (7, 71, 72) und deren Abtransport steuert. 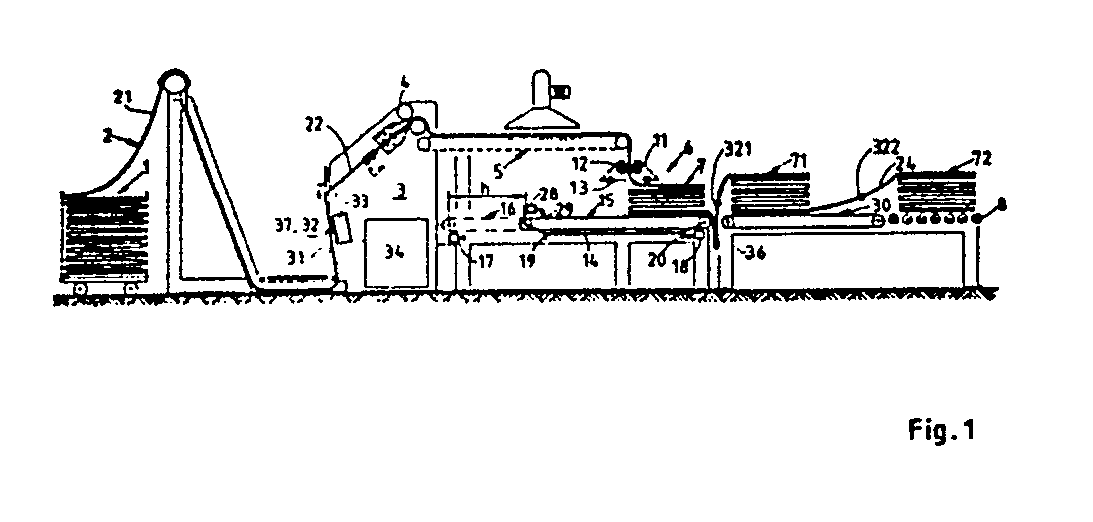
Description
Bahnen aus Textilgewebe, Strickwerk und aus textilartigem Werkstoff wie sie etwa unter dem Begriff "non woven" bekannt sind, werden in der Regelnach Abschluß ihrer substantiellen Fertigstellung durch eine Legevorrichtung in Faltenstapel gelegt und in dieser Form der weiteren Verarbeitung zugeführt. Da jedoch die Kapazität der Herstellungsmaschinen solcher Textilbahnen wie Strickmaschinen und dergleichen begrenzt ist, haben auch die auf solche Weise gefertigten Textilbahnen nur eine begrenzte Länge. Daher sind die vornehmlich thermischen Behandlungszyklen, aber auch chemische Behandlungsvorgänge nur für kurze Zeitspannen auszuführen, oder man muß die Anlage stillsetzen, um eine neue Textilbahn einführen zu können. Auf diese Weise werden nicht nur die Bearbeitungszeit verlängert und die Herstellungskosten vergrößert, sondern es kann auch durch unkontrolliert lange Einwirkungen von Bearbeitungsmedien zu teils erheblichen Qualitätsminderungen, oftmals zu Ausschuß kommen.Sheets of textile fabric, knitting and of textile-like material, such as are known under the term "non-woven", are placed in a stack of folds after completion of their substantial completion by means of a laying device and are fed in this form for further processing. However, since the capacity of the production machines of such textile webs such as knitting machines and the like is limited, the textile webs produced in this way also have a limited length. Therefore, the primarily thermal treatment cycles, but also chemical treatment processes can only be carried out for short periods, or the system must be shut down in order to be able to introduce a new textile web. In this way, not only is the processing time extended and the manufacturing costs increased, but uncontrolledly long exposure to processing media can sometimes lead to considerable quality reductions, often to rejects.
Die Erfindung geht aus von dem eingangs definierten Verfahren und verfolgt die Aufgabe, dieses Verfahren in solcher Weise weiterzubilden, daß ein Umsetzen oder Neueinführen von Textilbahnen während der Funktionsdauer einer verfahrenstechnischen Behandlung weitgehend vermieden wird.The invention is based on the method defined at the outset and pursues the task of developing this method in such a way that the implementation or reintroduction of textile webs is largely avoided during the functional period of a process engineering treatment.
Zur Lösung dieser Aufgabe werden erfindungsgemäß mehrere kürzere Textilbahnen mit ihren Enden zu einer einzigen langen Textilbahn verbunden, und daraufhin wird die lange Textilbahn in kontinuierlichem Durchlauf einer verfahrenstechnischen Behandlung unterworfen und anschließend in Einheiten der kürzeren Textilbahnen gefaltet und in Stapeln abgelegt.To achieve this object, several shorter textile webs are connected according to the invention with their ends to form a single long textile web, and then the long textile web is subjected to a process-related treatment in a continuous pass and then folded in units of the shorter textile webs and stored in stacks.
Im Prinzip können die kurzen Textilbahnen unmittelbar nach Fertigstellen der einzelnen Faltenstapel voneinander getrennt werden, aber hierzu besteht keine Notwendigkeit, d.h. man kann die noch zusammenhängenden Faltenstapel weiter fördern und gegebenenfalls einer weiteren kontinuierlichen oder schrittweisen Behandlung unterziehen.In principle, the short textile webs can be separated from one another immediately after the individual fold stacks have been completed, but there is no need for this, i.e. the stack of folds still connected can be conveyed further and optionally subjected to a further continuous or step-wise treatment.
Auf diese Weise wird eine eingesetzte Textilbahn bis zum Auslauf ihres Endes durch die ganze Anlage ohne jeden Stillstand hindurchgefördert. Der Werkstoff kann daher weder durch Überhitzen noch durch andere überlange Einwirkung eines Mediums eine Änderung erfahren.In this way, an inserted textile web is conveyed through the whole system without any standstill until its end. The material can therefore not change due to overheating or other excessive exposure to a medium.
Nach einer Weiterbildung der Erfindung werden an oder mit fester Zuordnung zu den Verbindungsstellen zwischen benachbarten Kurzbahnen berührungslos abstastbare Signalelemente eingearbeitet, deren Vorhandensein an einer vorgegebenen Durchlaufstelle der Langtextilbahn abgetastet und für Steuerungszwecke zum Legen der Textilbahn und Weiterfördern der so gebildeteten Faltenstapel herangezogen wird. Auf diese Weise gehen die Steuerimpulse grundsätzlich von der zu bearbeitenden Textilbahn aus, insbesondere aus dem Bereich der Verbindungsstellen zwischen benachbarten Kurzbahnen. Dabei ist es zwar erwünscht, aber nicht notwendig, daß diese Kurzbahnen gleiche Länge haben und auch die Signalelemente immer in bestimmter Weise der Verbindungsstelle zugeordnet sind. Um einen vollständig automatischen Betrieb zu ermöglichen, sollte aber der Abstand zwischen der Taststelle für das Signalelement und der Legevorrichtung vermessen und auf eine ganze Mehrzahl von Faltenbreiten beziehungsweise Legelängen abgestimmt werden.According to a further development of the invention, contactlessly scannable signal elements are incorporated on or with a fixed assignment to the connection points between adjacent short paths, the presence of which is sensed at a predetermined passage point of the long textile path and used for control purposes for laying the textile path and further conveying the fold stacks thus formed. In this way, the control impulses generally originate from the textile web to be processed, in particular from the area of the connection points between adjacent short webs. It is desirable, but not necessary, that these short paths have the same length and that the signal elements are always assigned to the connection point in a certain way. In order to enable fully automatic operation, the distance between the touch point for the signal element and the laying device should be measured and matched to a large number of pleat widths or laying lengths.
Dies ermöglicht auch eine bestimmte Einordnung des Signalelementes in der Bahn zwischen benachbarten Warenstapeln.This also enables the signal element to be arranged in a certain way in the web between adjacent stacks of goods.
Zweckmäßigerweise wird mit dem Legen eines neuen Stapels begonnen, wenn die Verbindungsstelle mit dem Signalelement so weit über den Legebereich hinausgelangt ist, daß sie jeweils mit Abstand zwischen zwei benachbarte Faltenstapel zu liegen kommt. An dieser Stelle läßt sich dann die Bahn nach Bedarf durchschneiden, um die einzelnen im übrigen unversehrten Kurzbahnen unterschiedlichen Weiterbehandlungen zuzuführen.It is useful to start laying a new stack when the connection point with the signal element has reached so far beyond the laying area that it comes to lie at a distance between two adjacent fold stacks. At this point, the web can then be cut as required in order to supply the individual, otherwise undamaged, short webs to different further treatments.
Die Erfindung betrifft ferner eine Vorrichtung zum Falten und Legen von Textilbahnen in Stapeln, wobei mehrere kürzere Textilbahnen mit ihren Enden zu einer einzigen langen Textilbahn verbunden werden und daraufhin die lange Textilbahn mit kontinuierlichem Durchlauf in Einheiten der kürzeren Textilbahnen gefaltet und in Stapeln abgelegt wird, insbesondere nach einem vorgeschilderten Verfahren, wobei dicht an der Textilbahn mit vorgegebenem Abstand vor der Legevorrichtung ein Detektor zum Abtasten eines in wenigstens einer Verbindungsstelle oder mit bestimmter Zuordnung zu einer Verbindungsstelle in die Textilbahn eingearbeiteten Signalelementes für die Steuerung einer Legevorrichtung zur Bildung einzelner Faltenstapel und deren Abtransport in Zuordnung zu benachbarten Faltenstapeln angebracht ist.The invention further relates to a device for folding and laying textile webs in stacks, wherein a plurality of shorter textile webs are connected at their ends to form a single long textile web, and then the long textile web is folded with units of the shorter textile webs and placed in stacks, in particular, in a continuous pass According to a previously described method, close to the textile web with a predetermined distance in front of the laying device, a detector for scanning a signal element incorporated in at least one connecting point or with a specific assignment to a connecting point in the textile web for controlling a laying device for forming individual fold stacks and their removal in Assignment to adjacent fold stacks is appropriate.
Die vom Detektor ausgelöste Steuerung kann dabei einen Programmspeicher mit einer Wähleinrichtung zum Vorwählen eines Arbeitsprogramms entsprechend der Beschaffenheit, der Abmessungen und der Behandlung der jeweiligen Textilbahn sowie des Transportweg-Abstandes zwischen Detektor und Legevorrichtung aufweisen.The controller triggered by the detector can have a program memory with a selection device for preselecting a work program in accordance with the nature, dimensions and treatment of the respective textile web and the distance of the transport path between the detector and the laying device.
Weitere Fortbildungen und Vorteile der Erfindung sind in den Ansprüchen festgehalten und der Beschreibung des Ausführungsbeispieles zu entnehmen, das jetzt anhand der Zeichnungen näher erläutert werden soll.Further developments and advantages of the invention are set out in the claims and can be found in the description of the exemplary embodiment, which will now be explained in more detail with reference to the drawings.
Es zeigen:
- Fig.1 eine schematische Seitenansicht einer Vorrichtung zum Bedämpfen, Kühlen bzw. Relaxieren und anschließenden Legen einer Textilbahn und die
- Fig.2-7 Teilansichten aus Fig.1 in verschiedenen Betriebsstellungen
- 1 shows a schematic side view of a device for steaming, cooling or relaxing and then laying a textile web and the
- Fig. 2-7 partial views from Fig. 1 in different operating positions
Nach Fig.1 wird aus einem Aufgabelager (1) eine meist schlauchförmige Textilbahn (2) abgezogen und durch einen Dämpfkalander (3) mit Kalanderwalzen (4) hindurch einer Kühlzone (5) und dann einer Legevorrichtung (6) zugeführt, die einzelne Faltenstapel (7) bildet, die in Zwischenabständen über eine Rollenbahn (8) weitergefördert werden. Die (lange) Textilbahn (2) setzt sich zusammen aus einzelnen kurzen Textilbahnen (21,22,23,24, usw).According to Fig. 1, a mostly tubular textile web (2) is drawn off from a feed store (1) and fed through a steaming calender (3) with calender rollers (4) to a cooling zone (5) and then to a laying device (6), the individual pleat stacks ( 7) forms, which are conveyed at intervals between a roller conveyor (8). The (long) textile web (2) is composed of individual short textile webs (21, 22, 23, 24, etc.).
Die Legevorrichtung (6) weist einen höhenverstellbaren Legeschlitten (11) mit Führungswalzen (12) und Bügelrollen (13) auf, sowie einen Legetisch (14) mit einem über diesen geführten Förderband (15).The laying device (6) has a height-adjustable laying carriage (11) with guide rollers (12) and bow rollers (13), and a laying table (14) with a conveyor belt (15) guided over it.
Der Legetisch (14) ist zwischen der mit vollen Linien ausgezogenen Vorwärtsstellung und mit der Strichpunktlinien eingezeichneten Rückwärtsstellung (16) hin- und hergehend verfahrbar und legt dabei einen der Faltenlänge entsprechenden Legehub h zurück. Dieser Legetisch (14) ist an eine endlose Kette angeschlossen, die zwischen zwei Umlenkrollen parallel zur Tischführung gespannt ist und ein Eingriffsteil wie einen Kulissenstein trägt, der in eine am Legeschlitten (11) vorgesehene, quer zur Schlittenführung verlaufende Kulissenführung greift. Der nicht gezeigte Antrieb des Transportbandes (15) wird einerseites gesteuert durch einen am Maschinengestell angebrachten Tisch-Endschalter (18), der von dem am Legetisch (14) angebrachten Anschlag (20) betätigt wird, und andererseits mittels eines am Legetisch (14) angebrachten Nockenschalters (28) durch in Abständen des Legehubes (h) am Förderband (15) selbst vorgesehene Nocken (29).The laying table (14) can be moved back and forth between the forward position drawn with full lines and the backward position (16) drawn in with the dash-dot lines and thereby covers a laying stroke h corresponding to the length of the folds. This laying table (14) is connected to an endless chain, which is tensioned between two deflection rollers parallel to the table guide and carries an engagement part such as a sliding block, which extends into a sliding guide provided on the laying slide (11) and runs transversely to the slide guide takes hold. The drive of the conveyor belt (15), not shown, is controlled on the one hand by a table limit switch (18) attached to the machine frame, which is actuated by the stop (20) attached to the laying table (14), and on the other hand by means of a attached to the laying table (14) Cam switch (28) by means of cams (29) provided on the conveyor belt (15) at intervals of the laying stroke (h).
Gestellfest ist wiederum das der Rollenbahn vorgeschaltete Abförderband (30) angeordnet, das zum Abfördervorgang über den am Maschinengestell angebrachten Tisch-Endschalter (17), mittels des am Legetisch (14) angebrachten Anschlages (19) eingeschaltet und in Bewegung gesetzt und über einen am Legetisch (14) angebrachten Nockenschalter (28) durch in Abständen des Legehubes h am Förderband (15) selbst vorgesehene Nocken (29) zum Stillstand gebracht wird.The removal conveyor belt (30) upstream of the roller conveyor is arranged in a frame-fixed manner, which is switched on and set in motion for the removal operation via the table limit switch (17) attached to the machine frame, by means of the stop (19) attached to the laying table (14) and via an on the laying table (14) attached cam switch (28) is brought to a standstill by cams (29) provided at intervals of the laying stroke h on the conveyor belt (15).
Die Bahnenden (31) der Kurztextilbahnen (21-24) sind in den Verbindungsstellen (37) fest miteinander verbunden, insbesondere quer zur Bahnrichtung vernäht. In der Naht oder wenigstens dicht an der Verbindungsstelle ist ein hier durch eine Verdickung der Bahn angedeudetes Signalelement (32) eingearbeitet, beispielsweise ein metallischer Faden. Da die Textilbahn (2) dicht an einem Detektor (33), beispielsweise einem UV-Detektor vorbeigeführt ist, gibt dieser stets dann ein Auslösesignal an die Steuerung (34).The web ends (31) of the short textile webs (21-24) are firmly connected to one another in the connection points (37), in particular sewn transversely to the web direction. A signal element (32), indicated here by a thickening of the web, is incorporated in the seam or at least close to the connection point, for example a metallic thread. Since the textile web (2) passes close to a detector (33), for example a UV detector, the latter always sends a trigger signal to the controller (34).
Sofern die Faltenstapel gleiche Höhe haben und jeweils einer einzigen Kurzbahn entsprechen sollen, erfordert dies gleiche Länge der Kurzbahnen (21-24). Zudem muß die Führungslänge zwischen dem Detektor (33) und einer Stelle im Bereich der Legevorrichtung einem ganzen Vielfachen der Faltenlänge bzw. des Legehubes (h) entsprechen. In der Regel reicht ein einmaliges Ausmessen, es können allerdings auch Verstellmittel zur Anpassung der wirklichen Fuhrungslänge an den Legehub vorgesehen sein.If the fold stacks are of the same height and each correspond to a single short path, this requires the same length of the short paths (21-24). In addition, the guide length between the detector (33) and a point in the area of the laying device must correspond to a whole multiple of the fold length or the laying stroke (h). As a rule, a single measurement is sufficient, but adjustment means can also be provided to adapt the actual guide length to the laying stroke.
Wie die Figuren 1 und 2 erkennen lassen, entspricht diese Wegstrecke etwa der halben Länge der Kurztextilbahn (22), und der zweite Signalgeber (321) hängt in einer Bahnschleife (36) zwischen den beiden Faltenstapeln (7) und (71), der vorangehende Signalgeber (322) zwischen den Faltenstapeln (71) und (72).As can be seen in FIGS. 1 and 2, this distance corresponds to approximately half the length of the short textile web (22), and the second signal transmitter (321) hangs in a web loop (36) between the two fold stacks (7) and (71), the preceding one Signal generator (322) between the fold stacks (71) and (72).
Damit nach der jetzt erfolgten Impulsgabe der Stapel (7) noch auf die gleiche Höhe wie die anderen Stapel (71) und (72) gebracht werden kann, muß die Textilbahn noch um eine aus dem Aufgabespeicher entnehmbare einfache oder mehrfache ganze Faltenlänge weitergefördert und abgelegt werden. Wenn die Verbindungsstelle (37) mit dem Signalelement (32) sich dem Stapel (7) gemäß Fig.3 bis auf ein bis zwei Faltenlängen h genähert hat, so wird bei Betätigen des hinteren Tischschalters (17) eine Folgeschaltung ausgelöst und dadurch das Abförderband (30) mit der gleichen Geschwindigkeit wie der Legetisch (14) in Bewegung gesetzt. Wird nun entsprechend Fig.5 in einer Anschlußstellung zum Abförderband (30) noch der vordere Tischschalter (18) betätigt, so bleibt der Legetisch (14) in dieser rechten Endstellung stehen. Gleichzeitig wird das auf dem Legetisch (14) befindliche Förderband (15) mit der gleichen Geschwindigkeit wie das Abförderband (30) in Bewegung gesetzt, wobei die Nocke (29) vom Bandschalter (28) abläuft, der Faltenstapel (7) auf das Abförderband (30) überführt und der Stapel (71) vom Abförderband auf die Rollenbahn (8) geschoben wird und den Stapel (72) weiterschiebt.In order for the stack (7) to be brought to the same height as the other stacks (71) and (72) after the momentum has now been given, the textile web has to be conveyed and deposited by a single or multiple whole fold length that can be removed from the feed store . If the connection point (37) with the signal element (32) has approached the stack (7) according to FIG. 3 to one or two fold lengths h, a sequential circuit is triggered when the rear table switch (17) is actuated, and the conveyor belt ( 30) set in motion at the same speed as the laying table (14). If, according to FIG. 5, the front table switch (18) is still actuated in a connection position to the conveyor belt (30), the laying table (14) remains in this right end position. At the same time, the conveyor belt (15) on the laying table (14) is set in motion at the same speed as the conveyor belt (30), the cam (29) running off the belt switch (28), the stack of folds (7) on the conveyor belt ( 30) transferred and the stack (71) is pushed from the conveyor belt onto the roller conveyor (8) and pushes the stack (72) onward.
Sobald der Bandschalter (28), nachdem die Nocke (29) abgelaufen ist, von der nächstfolgenden Nocke betätigt wird, kommt das Abförderband (30) zum Stillstand und der Legeschlitten (11) fährt in seine untere Ausgangslage. Das Förderband (15) läuft zur Bildung der Schlaufe (36) noch um eine Lagelänge weiter. Wird der Bandschalter (28) von der übernächstfolgenden Nocke betätigt, so bleibt das Förderband (15) stehen und der Legetisch (14) beginnt wieder hin- und herzufahren.As soon as the belt switch (28) is actuated by the next cam after the cam (29) has expired, the conveyor belt (30) comes to a standstill and the laying carriage (11) moves to its lower starting position. The conveyor belt (15) runs one layer length to form the loop (36). If the belt switch (28) is actuated by the next cam, the conveyor belt (15) stops and the laying table (14) begins to move back and forth.
Das Signalelement kann selbststrahlungsaktiv sein, es genügt aber die Eigenschaft der Ertastbarkeit durch irgendeinen der bekannten Detektoren.The signal element can be self-radiation active, but the property of tactility by any of the known detectors is sufficient.
Der nicht eingezeichnete Programmspeicher kann mit anderen Steuereinheiten in der Steuerung (34) zusammengefaßt sein, die ihren Auslöseimpuls vom Detektor (33) erhält. Auch der Programmwähler muß jede gleichende Ausbildung und Anordnung erfahren.The program memory (not shown) can be combined with other control units in the controller (34), which receives its trigger pulse from the detector (33). The program selector must also experience every similar training and arrangement.
Auf diese Weise können nahezu beliebig viele Kurzbahnen hintereinandergeschaltet, einer wie auch immer gearteten Behandlung unterworfen und anschließend abgetafelt werden, ohne daß Teile einer Kurzbahn einem anderen Faltenstapel zugeführt werden. Daher lassen sich grundsätzlich auch Textilbahnen hintereinanderschalten, die in mancherlei Hinsicht unterschiedlich beschaffen sind, solange sie durch die vorgesehene Behandlung nicht nachteilig verändert werden. Die einzelnen Faltenstapel können bis zur Konfektionierung zusammengeschlossen bleiben oder nach Bedarf an der Trennstelle bzw. einer Naht wieder voneinander gelöst werden.In this way, almost any number of short paths can be connected in series, subjected to any kind of treatment and then paneled without parts of a short path being fed to another fold stack. Therefore, in principle, textile webs can also be connected in series, which have different properties in many respects, as long as they are not adversely changed by the intended treatment. The individual fold stacks can be kept together until ready for assembly or can be detached from one another at the point of separation or a seam.
Claims (19)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3836974A DE3836974A1 (en) | 1988-10-31 | 1988-10-31 | METHOD AND DEVICE FOR FOLDING AND LAYING TEXTILE FILMS IN STACKS |
| DE3836974 | 1988-10-31 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0366980A2 true EP0366980A2 (en) | 1990-05-09 |
| EP0366980A3 EP0366980A3 (en) | 1990-06-06 |
| EP0366980B1 EP0366980B1 (en) | 1993-07-14 |
Family
ID=6366212
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP89118743A Expired - Lifetime EP0366980B1 (en) | 1988-10-31 | 1989-10-09 | Method and apparatus for continuous treatment of textile webs |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0366980B1 (en) |
| DE (2) | DE3836974A1 (en) |
| ES (1) | ES2041933T3 (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0768261A1 (en) * | 1995-10-12 | 1997-04-16 | Solipat Ag | Device and method for continuous zig-zag folding and stacking of web-shaped goods |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6155551A (en) * | 1997-12-19 | 2000-12-05 | Vmi Americas, Inc. | Reciprocating stacker for continuous strip material |
| FR3064938A1 (en) * | 2017-04-07 | 2018-10-12 | Compagnie Generale Des Etablissements Michelin | THE STACKING OF RUBBER MIXTURE PATCHES |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1219437B (en) * | 1954-12-04 | 1966-06-23 | Gillet Thaon Sa | Machine for folding and measuring webs of fabric |
| US3314844A (en) * | 1963-05-01 | 1967-04-18 | Hadley Company Inc | Fabric seam bonding |
| US3344230A (en) * | 1964-07-15 | 1967-09-26 | Heceivehs fos receiving a colour tele- vision signal including a frequency- modulated subcarrier | |
| US3607506A (en) * | 1968-08-28 | 1971-09-21 | Ford Motor Co | Process for continuously feeding separate lengths of sheet materials |
| DE2530963C2 (en) * | 1975-07-11 | 1984-03-01 | Jakob 4156 Willich Rüttgers | Device for stocking, in particular textile webs |
| US4027394A (en) * | 1975-11-12 | 1977-06-07 | Herbert Morantz | Drapery length marking device |
| SE412218B (en) * | 1978-07-12 | 1980-02-25 | Bonnierfoeretagen Ab | DEVICE FOR MAGAZINE PRESSURES |
| DE2949423C2 (en) * | 1979-12-08 | 1982-06-16 | Josef Jasper Gmbh & Co, 4282 Velen | Device for the wet treatment of strand or web-shaped textiles of limited length |
| DE3151897A1 (en) * | 1981-12-30 | 1983-07-07 | Norsel Textilmaschinen AG, 8280 Kreuzlingen | Method and device for treating spot-like zones, especially defects, in material webs |
| US4573958A (en) * | 1984-05-08 | 1986-03-04 | Biesinger Peter J | Cuttling machine for continuous input of web |
| US4670001A (en) * | 1985-12-13 | 1987-06-02 | Campbell Joseph I | Bottom stacking tray |
| DE3700402C1 (en) * | 1987-01-08 | 1988-07-07 | Hunkeler Ag Jos | Method and device for connecting the ends of two material webs |
-
1988
- 1988-10-31 DE DE3836974A patent/DE3836974A1/en not_active Withdrawn
-
1989
- 1989-10-09 ES ES198989118743T patent/ES2041933T3/en not_active Expired - Lifetime
- 1989-10-09 EP EP89118743A patent/EP0366980B1/en not_active Expired - Lifetime
- 1989-10-09 DE DE8989118743T patent/DE58904906D1/en not_active Expired - Fee Related
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0768261A1 (en) * | 1995-10-12 | 1997-04-16 | Solipat Ag | Device and method for continuous zig-zag folding and stacking of web-shaped goods |
| US5820539A (en) * | 1995-10-12 | 1998-10-13 | Solipat Ag | Device and method for continuous plaiting of web-shaped material |
Also Published As
| Publication number | Publication date |
|---|---|
| ES2041933T3 (en) | 1993-12-01 |
| EP0366980A3 (en) | 1990-06-06 |
| EP0366980B1 (en) | 1993-07-14 |
| DE3836974A1 (en) | 1990-05-03 |
| DE58904906D1 (en) | 1993-08-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE102007052594B4 (en) | Method and device for producing spiral sieves | |
| EP0510525B1 (en) | Method and device for handling printed products | |
| DE2531734C2 (en) | Thread guidance on loop-forming machines with revolving thread guides | |
| DE1208285B (en) | Insert folding device for laundry or the like. | |
| EP0387371B1 (en) | Process and device for cutting out pieces of clothing | |
| EP2028307A1 (en) | Method and device for placing a unidirectional thread ply on a longitudinal conveyor, method for laying weft threads on warp knitting machines, warp knitting machine and multi-axis machine | |
| DE3886521T2 (en) | DEVICE FOR HEMING ADAPTED TEXTILE SURFACES. | |
| DE2228159C3 (en) | Device for guiding and processing lengths of fabric | |
| DE3920659A1 (en) | Cloth inspection table | |
| EP3554752B1 (en) | Grid welding machine | |
| DE2153158A1 (en) | METHOD AND DEVICE FOR SLIDING A CLAMP ON FOLDED ARTICLES O.AE | |
| DE4244827C2 (en) | Feeding laundry items to mangle | |
| EP0366980B1 (en) | Method and apparatus for continuous treatment of textile webs | |
| EP0041685A1 (en) | Process and apparatus for joining metal or synthetic spiral elements into a belt | |
| DE2856871A1 (en) | PROCESS AND DEVICE FOR THE MANUFACTURING OF CONTINUOUSLY EMBROIDERED FABRICS | |
| DE1660905A1 (en) | Device for picking up and feeding pieces of fabric to a sewing machine | |
| EP0446625A1 (en) | Threading and thread changing device for thread-guides | |
| DE2653790C3 (en) | Device for laying patterned strips of fabric in layers | |
| AT391714B (en) | METHOD AND DEVICE FOR CROSS-CUTTING, DOUBLE-SIDED HEMING AND SEWING OF FLAT MATERIALS, IN PARTICULAR FROTTEEWARE | |
| EP0505318A1 (en) | Folding device for clothes | |
| CH635149A5 (en) | DAMPER FOR TREATING A CONTINUOUSLY CONTINUOUS TEXTILE TRACK, WHICH IS EXPOSED IN IT TO THE EFFECT OF REACTION AGENTS DURING A PARTICULAR DURATION. | |
| EP3369685A1 (en) | Device for transporting elongated pieces to a pick-up position and for depositing elongated pieces at this position | |
| DE2208756C3 (en) | Tensioning machine for material webs | |
| EP1129950B1 (en) | Apparatus for removing a bag from a stack of bags | |
| DE3737369C1 (en) | Sewing machine for pieces of fabric |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): CH DE ES FR IT LI |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): CH DE ES FR IT LI |
|
| 17P | Request for examination filed |
Effective date: 19900523 |
|
| 17Q | First examination report despatched |
Effective date: 19911213 |
|
| ITF | It: translation for a ep patent filed | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): CH DE ES FR IT LI |
|
| REF | Corresponds to: |
Ref document number: 58904906 Country of ref document: DE Date of ref document: 19930819 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2041933 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 19950914 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 19951003 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19951030 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19961010 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Effective date: 19961031 Ref country code: CH Effective date: 19961031 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19961221 Year of fee payment: 8 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19970630 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980701 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 19990503 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20051009 |