EP0409805B1 - Vorrichtung zum Dekontaminieren einer Giesskokille, die insbesondere für Titan und dergleichen verwendet wurde - Google Patents
Vorrichtung zum Dekontaminieren einer Giesskokille, die insbesondere für Titan und dergleichen verwendet wurde Download PDFInfo
- Publication number
- EP0409805B1 EP0409805B1 EP90830318A EP90830318A EP0409805B1 EP 0409805 B1 EP0409805 B1 EP 0409805B1 EP 90830318 A EP90830318 A EP 90830318A EP 90830318 A EP90830318 A EP 90830318A EP 0409805 B1 EP0409805 B1 EP 0409805B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- sealed chamber
- casting
- inert gas
- titanium
- chamber
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000005266 casting Methods 0.000 title claims description 54
- RTAQQCXQSZGOHL-UHFFFAOYSA-N Titanium Chemical compound [Ti] RTAQQCXQSZGOHL-UHFFFAOYSA-N 0.000 title claims description 15
- 239000010936 titanium Substances 0.000 title claims description 12
- 229910052719 titanium Inorganic materials 0.000 title claims description 12
- 238000005202 decontamination Methods 0.000 title claims description 7
- 230000003588 decontaminative effect Effects 0.000 title claims description 7
- 239000011261 inert gas Substances 0.000 claims description 18
- XKRFYHLGVUSROY-UHFFFAOYSA-N Argon Chemical compound [Ar] XKRFYHLGVUSROY-UHFFFAOYSA-N 0.000 claims description 12
- 229910052751 metal Inorganic materials 0.000 claims description 10
- 239000002184 metal Substances 0.000 claims description 10
- 239000001307 helium Substances 0.000 claims description 7
- 229910052734 helium Inorganic materials 0.000 claims description 7
- SWQJXJOGLNCZEY-UHFFFAOYSA-N helium atom Chemical compound [He] SWQJXJOGLNCZEY-UHFFFAOYSA-N 0.000 claims description 7
- 229910052786 argon Inorganic materials 0.000 claims description 6
- 239000000463 material Substances 0.000 claims description 6
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 claims description 5
- 229910052802 copper Inorganic materials 0.000 claims description 5
- 239000010949 copper Substances 0.000 claims description 5
- 239000011888 foil Substances 0.000 description 4
- 239000011248 coating agent Substances 0.000 description 3
- 238000000576 coating method Methods 0.000 description 3
- 238000011109 contamination Methods 0.000 description 3
- 238000007789 sealing Methods 0.000 description 3
- 238000009750 centrifugal casting Methods 0.000 description 2
- 239000007789 gas Substances 0.000 description 2
- 238000005495 investment casting Methods 0.000 description 2
- 238000000034 method Methods 0.000 description 2
- 239000011819 refractory material Substances 0.000 description 2
- 230000013011 mating Effects 0.000 description 1
- 239000000155 melt Substances 0.000 description 1
- 239000007769 metal material Substances 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 239000011148 porous material Substances 0.000 description 1
- 238000002360 preparation method Methods 0.000 description 1
- 239000000126 substance Substances 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D27/00—Treating the metal in the mould while it is molten or ductile ; Pressure or vacuum casting
- B22D27/15—Treating the metal in the mould while it is molten or ductile ; Pressure or vacuum casting by using vacuum
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D21/00—Casting non-ferrous metals or metallic compounds so far as their metallurgical properties are of importance for the casting procedure; Selection of compositions therefor
- B22D21/002—Castings of light metals
- B22D21/005—Castings of light metals with high melting point, e.g. Be 1280 degrees C, Ti 1725 degrees C
Definitions
- the present invention relates to a device for decontaminating casting moulds, particularly for titanium castings and the like.
- the present invention relates to a device of the said type, particularly suitable for titanium castings, which device allows the decontamination of the casting mould or cylinder to be realized before the latter is inserted into the casting machine, which greatly simplifies the realization and the operation of said castings, and allows casting articles with optimum characteristics to be obtained.
- investment castings are realized by making a wax model of the article to be obtained, which model is then recovered with a coating of a refractory material.
- the whole is subjected to a furnace heat treatement, during which the wax sublimes leaving a cavity corresponding to the piece to be obtained at the interior of the coating.
- the casting cylinder so obtained is placed at the interior of the casting machine.
- the first one has a centrifugal system and works on the basis of argon saturation without vacuum.
- the second kind of machine is based on argon saturation and it works under vacuum but without any centrifugal system.
- castings must have accurate fit, with very thin and strong margins.
- the first kind of casting machines (centrifugal casting machines) work by argon saturation of the casting chamber and the castings have thin margins and accurate fit, but metal will be contaminated because of absence of vacuum.
- the main problem for this kind of machines is that of obtaining the vacuum by sealing the centrifugal system. It is technically very difficult and, mainly, very much expensive.
- the second kind of machines (vacuum machines), not having the centrifugal system, allows to obtain castings without contamination, but it is impossible to get multiple castings with good thin margins.
- the Applicant of the present invention having well aware of the problems and needs mentioned above, has realized a device which allows all the drawbacks to be obviated, allowing a casting, particularly a titanium casting, to be realized, in a fully decontaminated environment and so an optimum quality article to be obtained.
- the device according to the present invention does not require the realization of complex sealing systems in the casting chamber of the casting machine, because in said chamber neither the inlet of the inert gases, nor, least of all, a vacuum are to be realized.
- the device according to the invention is used with a centrifugal system and provides an adequate vacuum with helium as the only residual gas.
- the decontamination is realized outside of the casting chamber, in an environment of a reduced size as compared to that of the casting chamber, and the device so prepared is directly placed into the chamber.
- the molten metal flow from the crucible onto the foil and melts it, and is kept in a decontaminated environment, under a vacuum, at the interior of which it is sucked off realizing an impurity-free casting.
- a device for decontamination the casting mould particularly for titanium castings and the like, which device comprises a sealed chamber, at the interior of which the casting cylinder is placed, said device being also endowed on its upper side with a means for the connection to an inert gas reservoir and with a vacuum source, and on the lower side with a thin sheet of a material that doesn't contaminate the metal to be cast, and having a thickness that allows it to withstand the vacuum made at the interior of the sealed chamber, and proportional to the mass of the casting metal, said sealed chamber having at least one removable extremity for allowing the casting cylinder to be introduced and, subsequently, to be taken out, and for allowing the next casting to be prepared.
- Said means for the connection to the inert gas reservoir and to the vacuum source may consist, according to the present invention, of a closing and opening valve or of a copper pipe, arranged between an opening made in the sealed chamber and the inert gas reservoir and the vacuum source, which pipe is cut, by crushing its extremities, after having realized the decontamination, so hermetically closing the device itself.
- said sealed chamber has an upper portion which is removable by threading or other analogous systems.
- the sealed chamber may have the lower portion as the only removable portion, or both portions may be removable, with systems analogous to those mentioned above.
- said thin sheet is made up of a titanium foil.
- Said thin sheet may also be made up of a plastic material.
- the inert gas employed is helium or argon, particularly helium.
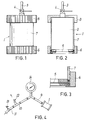
- the device 1 provides a cylindrical chamber 2, at the interior of which the casting cylinder is placed, which chamber is hermetically closed and endowed on the upper side with a small connection tube 3 endowed with an opening and closing valve 4.
- the lower wall of the chamber 2 consists of a thin sheet 5 of titanium, or of an other non-contaminating plastic or metallic material, of such a thickness as to melt, at the interior of the casting chamber of the casting machine, owing to the metal poured from the crucible, and, moreover, as to withstand the vacuum made at the interior of the chamber 2.
- the device 1 is realized with the lower portion 6 which is unscrewable with respect to the main body 7, so that the foil 5 may be replaced and the device reemployed.
- the upper portion 8 is also unscrewable with respect to the main body 7.
- the device 1 may be also realized with the body 7 and the lower portion 6 which are integral to each other. In this case, the whole assembly body 7, the lower portion 6, and the thin sheet or foil 5 must be replaced to employ the device itself again.
- the matings between the body 7 and the lower portion 6 and the upper portion 8, realized in such a way, as to insure an absolute seal, may also be realized in a different way with respect to the interthreading system shown in the figure.
- valves 12 and 13 are provided for excluding either or both of them during the preparation cycle.
- a pressure gauge 14 is provided on the tube 9.
- the small tube 3 is attached to the tube 9 and the valve 4 is opened. Then an inert gas, preferably helium, is let into chamber 2, and then a vacuum is made.
- an inert gas preferably helium
- valve 4 is closed.
- the chamber 2 with the casting cylinder is now in a decontaminated environment under vacuum, at the interior of which an optimum casting is obtained.
- the device 1 is then ready for being placed into the casting machines.
- the device 1 according to the present invention may be connected to the inert gas reservoir and to the vacuum source by means of a copper tube provided on an opening of chamber 2 (which opening is realized in place of valve 4).
- the closing and opening valve will be provided on the inert gas delivering and vacuum-making facility.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacture And Refinement Of Metals (AREA)
- Filling Or Discharging Of Gas Storage Vessels (AREA)
- Furnace Details (AREA)
Claims (12)
- Vorrichtung zum Dekontamination einer Giesskokille, insbesondere zum Giessen von Titan und olrgl., dadurch gekennzeichnet, dass die Vorrichtung eine dicht gesohlossene Kammer (2) enthaelt, in der die Giesskokille angeordnet its und die an ihrer Oberseite mit Verbindungsmitteln (3,4) zur Verbindung mit einem Inertgasbehalter und mit einer Vakuumquelle und an ihrer Unterseite mit einer duennen Folie (5), die aus einem das zu giessende Metalschmelze nicht kontaminierenden Material besteht und eine zum Aushalten des im Inneren der Kammer (2) herschenden, Vakuums genuegende und zur Giessmasse des Titans proportionale Dicke hat, wobei mindestens ein Ende der Kammer (2) abnehmbar ist, um das Einfuehren und Abfuehren der Giesskokille sowie die Vorbereitung des naechsten Giessvorganges zu gestatten.
- Vorrichtung nach Anspruch 1, dadurch gekennzeichnet, dass die vorgenannten Mittel (3,4) zur Verbindung mit dem Inertgasbehaelter und mit der Vakuumquelle aus einem ein- und ausschaltbaren Ventil (4) bestehen.
- Vorrichtung nach Anspruch 1, dadurch gekennzeichnet, dass die vorgenannten Mittel (3,4) zur Verbindung mit dem Inertgasbehalter und mit der Vakuumquelle aus einem Kupferrohr (3) bestehen, dessen ein Ende an eine Oeffnung der Dichtkammer (2) angeschlossen und das andere Ende mit dem Inertgasbehaelter und der Vakuumquelle verbunden ist, wobei das Kupferrohr nach der Dekontamination abgeschnitten wird, um somit die Dichtkammer dicht zu schliessen.
- Vorrichtung nach je einem der Ansprueche 1 bis 3, dadurch gekennzeichnet, dass der Oberteil (8) der Dicktkammer (2) abnehmbar ist.
- Vorrichtung nach je einem der Ansprueche 1 bis 3, dadurch gekennzeichnet, dass die Dichtkammer einen abnehmbaren unteren Teil hat.
- Vorrichtung nach je einem den Ansprueche 1 bis 3, dadurch gekennzeichent, dass die beiden Unter- und Oberteil (6 bzsw. 8) der Dichtkammer abnehmbar sind.
- Vorrichtung nach je einem der Ansprueche 2 bis 6, bei der die vorgenannten Unter- und Oberteil (6 bzsw. 8) mit der Dichtkammer (2) durch Verschraubung gekuppelt sind.
- Vorrichtung nach je einem der Ansprueche 2 bis 6, bei der die vorgenannten Unter- und Oberteil (6 bzsw. 8) mit der vorgenannten Dichtkammer (2) durch eine dichtende Rastkupplung verbunden sind.
- Vorrichtung nach je einem der Ansprueche 2 bis 6, dadurch gekennzeichnet, dass die duenne Folie (5) eine Titanfolie ist .
- Vorrichtung nach je einem der Ansprueche 1 bis 8, dadurch gekennzeichnet, dass die genannten Folie (5) aus einem Kunststoff besteht.
- Vorrichtung nach je einem der vorhergehenden Ansprueche, dadurch gekennzeichnet, dass das vorgenannte Inertgas Helium ist.
- Vorrichtung nach je einem der Anspruech 1 bis 10, dadurch gegenzeichnet, dass das vorgenannte Inertgas Argon ist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT8948199A IT1231483B (it) | 1989-07-18 | 1989-07-18 | Dispositivo per la decontaminazione di uno stampo di fusione, in particolare per fusioni di titanio e simili |
| IT4819989 | 1989-07-18 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0409805A1 EP0409805A1 (de) | 1991-01-23 |
| EP0409805B1 true EP0409805B1 (de) | 1993-11-10 |
Family
ID=11265165
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP90830318A Expired - Lifetime EP0409805B1 (de) | 1989-07-18 | 1990-07-10 | Vorrichtung zum Dekontaminieren einer Giesskokille, die insbesondere für Titan und dergleichen verwendet wurde |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0409805B1 (de) |
| JP (1) | JP3070933B2 (de) |
| DE (1) | DE69004512T2 (de) |
| IT (1) | IT1231483B (de) |
Family Cites Families (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3682458A (en) * | 1969-12-29 | 1972-08-08 | Trw Inc | Melting of refractory and reactive metals |
| US4007772A (en) * | 1974-11-06 | 1977-02-15 | Laedtke Donald O | Apparatus for vacuum precision casting |
| GB2170742B (en) * | 1985-01-31 | 1988-04-07 | Maio Spa Mario Di | Apparatus for use in producing castings by the }lost-wax} method |
-
1989
- 1989-07-18 IT IT8948199A patent/IT1231483B/it active
-
1990
- 1990-07-10 EP EP90830318A patent/EP0409805B1/de not_active Expired - Lifetime
- 1990-07-10 DE DE90830318T patent/DE69004512T2/de not_active Expired - Fee Related
- 1990-07-18 JP JP2190365A patent/JP3070933B2/ja not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| JP3070933B2 (ja) | 2000-07-31 |
| IT1231483B (it) | 1991-12-07 |
| DE69004512D1 (de) | 1993-12-16 |
| JPH03174969A (ja) | 1991-07-30 |
| DE69004512T2 (de) | 1994-04-21 |
| EP0409805A1 (de) | 1991-01-23 |
| IT8948199A0 (it) | 1989-07-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2100832C (en) | Method and apparatus for making intermetallic castings | |
| DE3815828C2 (de) | ||
| CA2028655A1 (en) | Apparatus and process for countergravity casting of metal with air exclusion | |
| US5559827A (en) | Vacuum melting-pressure pouring induction furnace | |
| JPH035277B2 (de) | ||
| US4254817A (en) | Metal casting apparatus | |
| US5168917A (en) | Casting of dental metals | |
| KR100801815B1 (ko) | 반중량 주조 방법과 그 장치 | |
| KR20010107613A (ko) | 경금속 주물, 특히 마그네슘 및 마그네슘 합금의 부품을제조하기 위한 방법 및 장치 | |
| JPS55165266A (en) | Pressure vaccum suction casting device utilizing high-frequency heating | |
| EP0409805A1 (de) | Vorrichtung zum Dekontaminieren einer Giesskokille, die insbesondere für Titan und dergleichen verwendet wurde | |
| GB2113587A (en) | Die casting process and apparatus therefor | |
| EP0190680A3 (de) | Verfahren und Giessanlage für die Herstellung von Metallgussstücken | |
| ITTO20010288A1 (it) | Apparecchiatura per il trasferimento di metalli liquidi da un contenitore di prelievo ad un contenitore di raccolta. | |
| JPS613653A (ja) | シ−ル機構を有するスライデイングノズル装置 | |
| CA1209781A (en) | Self-tapping support for shell molds | |
| JPH11192541A (ja) | アルミニウム合金の鋳造装置 | |
| ATE125476T1 (de) | Giessvorrichtung und verfahren. | |
| EP1082187B1 (de) | Feingiessen unter verwendung einer abdichtbaren druckkappe | |
| EP0018450B1 (de) | Giessvorrichtung | |
| EP0844966A4 (de) | Verfahren und vorrichtung zum vergiessen von materialschmelzen | |
| JPS5844312B2 (ja) | 溶融金属試料採取装置 | |
| JPH038256Y2 (de) | ||
| JPS5731463A (en) | Casting method for thin walled casting | |
| US4887661A (en) | Casting mold for foundry castings |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): CH DE ES FR GB IT LI SE |
|
| 17P | Request for examination filed |
Effective date: 19910606 |
|
| 17Q | First examination report despatched |
Effective date: 19920522 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| ITF | It: translation for a ep patent filed | ||
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): CH DE ES FR GB IT LI SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19931110 Ref country code: LI Effective date: 19931110 Ref country code: ES Free format text: THE PATENT HAS BEEN ANNULLED BY A DECISION OF A NATIONAL AUTHORITY Effective date: 19931110 Ref country code: CH Effective date: 19931110 |
|
| REF | Corresponds to: |
Ref document number: 69004512 Country of ref document: DE Date of ref document: 19931216 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19940710 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19940710 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19950629 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19970328 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20000628 Year of fee payment: 11 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020501 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050710 |