EP0410501B1 - Wirbelbett zum Abschrecken von Stahldrähten - Google Patents
Wirbelbett zum Abschrecken von Stahldrähten Download PDFInfo
- Publication number
- EP0410501B1 EP0410501B1 EP90201864A EP90201864A EP0410501B1 EP 0410501 B1 EP0410501 B1 EP 0410501B1 EP 90201864 A EP90201864 A EP 90201864A EP 90201864 A EP90201864 A EP 90201864A EP 0410501 B1 EP0410501 B1 EP 0410501B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- fluidized bed
- cooling
- temperature
- wires
- convection cooler
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/52—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for wires; for strips ; for rods of unlimited length
- C21D9/54—Furnaces for treating strips or wire
- C21D9/56—Continuous furnaces for strip or wire
- C21D9/567—Continuous furnaces for strip or wire with heating in fluidised beds
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/74—Methods of treatment in inert gas, controlled atmosphere, vacuum or pulverulent material
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/52—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for wires; for strips ; for rods of unlimited length
- C21D9/54—Furnaces for treating strips or wire
- C21D9/56—Continuous furnaces for strip or wire
- C21D9/573—Continuous furnaces for strip or wire with cooling
- C21D9/5732—Continuous furnaces for strip or wire with cooling of wires; of rods
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/52—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for wires; for strips ; for rods of unlimited length
- C21D9/54—Furnaces for treating strips or wire
- C21D9/64—Patenting furnaces
Definitions
- the invention relates to an installation adapted for continuous quenching of steel wires to a temperature of 250°C at the lowest, having a fluidized bed cooling chamber.
- a fluidized bed cooling chamber comprises a container that is filled to a certain height with granules for forming the fluidized bed.
- the granules are inert to high temperatures of 1500°C and more.
- At the bottom of the granule bed there is an inlet adapted for blowing a carrying gas upwards into the bed, with an input flow that is as equally as possible distributed over the bottom surface of the bed.
- Typical grain materials are silica-, almumina-, or zirconiasand, silicon carbide or ferrosilicon, and typical grain dimensions lie in the range between 0.03 and 0.5 millimeter and typical fluidized bed heights for wire applications lie around 0.3 - 0.6 meter.
- the blowing speed into the bed for fluidization thereof depends on the chosen grain type, and typical speeds lie in the range between 0.06 and 0.15 m/sec.
- the cooling medium receives a heat transmission coefficient towards the wires of the order of 200 to 600 W/m°K, which already comes near to the coefficient for cooling liquids. With such cooling medium it is then possible to quench steel wires i.e. to cool with a speed of more than 200°C per second.
- the fluidized bed cooling chamber is further provided with the necessary wire guiding and access means to guide the wire in and out the fluidized bed.
- the fluidized bed cooling chamber will be arranged for simultaneous and continuous treatment of a number of wires (typical quantities are 10 to 50), which pass side by side through the fluidized bed, in the axial direction of the wires.
- Typical wire thicknesses vary from 1 to 6 millimeter, and typical carbon contents lie in the range from 0.05 to 1%.
- Such a fluidized bed has to maintain its quenching temperature. This means that the quantity of heat that enters the bed via the hot wires and that is given off to the cooling fluid, must also be carried off with the same speed from the fluid. In a fluidized bed, this occurs via the carrying gas that is blown in at a comparatively low temperature, that then takes over the heat from the grains, and that then leaves the bed at the top of it at a higher temperature.
- the temperature of the fluidized bed is kept as a constant value (notwithstanding any disturbancies in the traveling speed and entrance temperature of the wires, and other disturbancies) by a regulator of the temperature that influences the entrance temperature of the carrying gas, as described in EP 195.473 (publication number). From the same document it is also known to additionally cool the fluidized bed by means of a propely system of water cooling pipes that are immersed in the fluidized bed, or by means of blowers that blow cooling air above the fluidized bed.
- Such fluidized bed is however limited with respect to its production capacity (i.e. kg of wire treated per second) per square meter of bed surface, so that a large production also needs a comparatively large fluidized bed.
- the primary cooling by the carrying gas is limited indeed, because the speed of the carrying gas through the bed cannot be forced up above values above 0.15 - 0.20 m/sec because the grains would then be blown out of the bed. Consequently, the flow input (m3/sec) per square meter of surface (is equal to the speed) has a limit, and the maximum possible difference between entrance and exit temperature of the carrying gas has also a limit that is mainly determined by the imposed quenching temperature.
- the startery cooling must be limited, because the water pipes cause a disturbance in the fluidization, and if there are too many of them, the fluidized bed appears rapidly to block up and to collapse.
- air blow cooling is used above the bed, then the heat drain capacity of the air is too small, and when this air is mixed up with atomized water, then it appears that this causes the upper surface of the bed to cake together.
- three measures are combined with each other : markedly increasing the density of the pipe system (indirect convection cooling), using a pipe system with air instead of water, and transferring the temperature control from the primary to the secondary cooling circuit.
- the density of the pipe system is consequently at least such, that its external surface where the cooling by convection of the fluidized bed occurs, takes at least 0.40 m per square meter bed surface, and preferably at least 0.80 m. And it is intended, when in use, to send a nominal air flow through it which causes a cooling capacity (KW/m bed surface) of the convection cooler that amounts to at least twice, and preferably four times, the cooling capacity of the primary cooling by the carrying gas.
- the depoty cooling system mustnot necessarily have the form of a number of pipes, but can also take other forms, in so far as the system is based on indirect convection cooling, i.e. cooling through a separating wall with convection on either side thereof.
- the control of the temperature of the fluidized bed is transferred from the primary cooling circuit, with the carrying gas, to the startery cooling circuit, with the indirect convection cooling with air.
- This is now easily feasible by control of the air flow that can be obtained at cold temperature and without any limit from the ambient air.
- Flow control of a water cooling system is much more difficult because this is continuously disturbed by steam formation. Due to the fact that according to said first measure, the bulk of the cooling has been transferred from the primary to the propely circuit, the steering with the propely cooling, from zero to the nominal cooling capacity, provides a very strong regulating system for the temperature.
- the cooling capacity of the convection cooler fed with air that is sucked in by a ventilator, can further be increased by injecting, in the air stream through the convection cooler, either in the cooler itself or in the supply duct, an atomized liquid, preferably water. Then it is possible to regulate the temperature of the bed by varying the flow, either of the cooling air, or of the liquid injection, or both. In fact, by acting on the injection of an atomized liquid, the specific heat C p of the cooling air is controlled. This specific heat is at its lowest level when the air is completely dry, but by injection of an atomized liquid, the vaporizing heat for the very small drops per unit of volume is added.
- the convection cooler has an inlet that is connected with an air source, and the specific heat flow H of the air stream through the convection cooler is variable, and the convection cooler comprises a regulator for keeping the fluidized bed temperature at a constant value, by varying said specific heat flow.
- Such a regulator will consequently, according to the general principles in control engineering, comprise a feeling device of the temperature of the fluidized bed, that produces a signal that is representative for that temperature, and a comparator, where said temperature is compared with an adjusted desired temperature and where a correction signal is generated that is representative of the observed deviation, to which is possibly added the integral and/or the derivative over the time of such difference (in the well-known P, PI, PD or PID regulating systems), and a correcting device where said correction signal is transformed into a variation of a magnitude by means of which the temperature is regulated (in this case the flow of air and/or the liquid injection).
- the system according to the invention and in which the fluidized bed is kept in a non-oxydising athmosphere, and in which the carrying gas comes from a furnace with uncomplete combustion, is extremely adapted for the quenching operation when continuously patenting steel wires.
- the wire is firstly continuously passed through an austenitizing furnace, in which the wire is heated up to a temperature ranging between 900°C and 1050°C, and then, on exit from the austenitizing furnace, is immediately quenched to a temperature ranging from 530°C to 570°C.
- the exhaust gas of the austenitizing furnace is used.
- the maximal heat drain capacity of the carrying gas per m of bed surface is limited to about 25 KW.
- the bed Owing to the presence of the strong depoty convection cooling, it is not necessary to design the bed for maximal cooling, so that a larger freedom exists for the design, and the bed can be designed for a heat drain of 10 to 15 KW per m bed surface.
- the nominal flow of the propely air cooling is then designed to a value that amounts to more than four times the above value, for instance five times, and in any case more than 50 KW/m, for instance 75 KW/m.
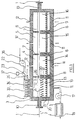
- Figure 1 shows a fluidized bed installation that is used for the continuous patenting of a row of steel wires 1, that are traveling side by side in the axial direction of the wires, i.e. in the direction of arrow 2.
- the row of steel wires is located in a single plane, perpendicular to the plane of the drawing, only one wire is visible.
- Figure 2 which is a partial view from the top, the parallel wires 1 are all visible.
- the whole of the fluidized bed installation consists of four fluidized bed chambers, 3, 4, 5 and 6 respectively, which are separated from each other by partitions 7 and 8, and which immediately follow the one after the other in downstream direction of the wires.
- the first chamber serves for quenching the entering wires, from a temperature inside the austenitizing range (depending on the steel and the desired final characteristics for the wire, this range lies in general between 900°C and 1050°C) to the patenting temperature, i.e. the temperature at which the formation of a fine sorbitic structure can start (depending on the steel and the desired final characteristics for the wire, this range lies in general between 530°C and 570°C). It is in this first chamber that the quenching has to occur, and where the problems arise that form the basis for the present invention, and consequently, it is this first chamber that is executed as an installation according to the invention.
- the second, third and fourth chamber serve to keep the wire at the patenting temperature during the time, necessary to allow the transformation into sorbite.
- the temperature of each chamber can be regulated to a temperature that must not necessarily be the same for the four chambers.
- the temperature difference can in theory be zero, or the fluidized bed temperature slightly higher, in order to compensate the radiation losses.
- the temperature in the last three chambers must not necessarily be the patenting temperature to which the wire was quenched in the first chamber, but can diverge therefrom by 30°C below or above said temperature, depending on the metallographic structure, aimed at for the sorbite.
- the length of the chambers may differ, and the number of chambers may vary from 2 to 8 or more.
- the whole of the fluidized bed installation is surrounded by a casing 9, that separates the fluidized bed chambers 3 to 6 as much as possible from the external athmosphere, with the exception of the slit openings 10 for the entrance and the exit of the row of wires 1 in and out the inside part of the installation, and of the inlet and outlet openings 11, respectively 12, for the carrying gas of each fluidized bed chamber separately.
- the four fluidized bed chambers 3 to 6 each comprise a fluidized bed 13 to 16 respectively, that is filled with grains of aluminium oxide with a grain size ranging between 0.03 and 0.5 mm, and in fluidized state, this bed reaches a height that in general is chosen between 0.3 and 0.6 meter, depending on the desired time for keeping the carrying gas in contact with the fluidized bed grains.
- the temperature to which the fluidized bed of the first chamber has to be regulated depends on the required cooling speed of the steel, i.e. on the diameter of the wires and their traveling speed, so that the cooling can penetrate to the core of the wire during the short dwelling time of the wire in the first chamber. For the traveling speeds used in this example, a temperature is taken around the value (500°C - 40d) in which d is the diameter of the wire in mm.
- the fluidized bed of the first chamber has a length, in the direction of the wires, of 1.10 m and a width of 1 meter, and the maximal number of wires that can be guided through this fluidized bed depends on the maximum heat drain capacity of the fluidized bed and on the diameter of the wires.
- the maximum total heat drain capacity has been designed for 105 KW, which corresponds with a capacity of quenching of maximum 1500 kg of steel per hour in the patenting operation, and this has to be taken into account when choosing the number of wires with a given diameter. In such choice it is also necessary to take into account the necessary dwelling time of the wire in the first chamber, which is inversely proportional to the diameter of the wire.
- this sytem will have a traveling speed of about 0,475 m/sec, and will be capable to treat up to 30 parallel wires at a maximum heat drain capacity of 105 KW.
- the system for guiding the wire through the fluidized bed has been designed for guiding 30 wires of a diameter of 1 to 6 mm. In the case of larger diameters, less than 30 wires shall then be treated in parallel, in order not to exceed the maximum designed production capacity.
- the exhaust gas is taken of a furnace (not shown), that is located immediately upstream, with respect to the wire movement, before the fluidized bed installation of Figure 1, which furnace is traversed by the same wires in order to be brought at an austenitizing temperature (between 900 and 1050°C). In this furnace, combustion takes place with a shortage of oxygen, so that this carrying gas cannot provoke any oxydation of the wire.
- the exhaust gas is sucked by a ventilator 17 via a heat exchanger 18, and is further blown through to the first fluidized bed 3.
- the exhaust gas is cooled down to about 150°C, and this gas is then blown in, via inlet 11 of the fluidized bed 3, in the plenum chamber 19 subjacent to fluidized bed 13.
- the plenum chamber 19 is separated from the fluidized bed 13 by the bottom 20 of fluidized bed chamber 3, and this bottom is provided with a multiplicity of blowing orifices 21, through which the carrying gas is blown, from the plenum chamber into the fluidized bed chamber, in a way, uniformly distributed over the bottom surface, and at a temperature of about 120°C.
- blowing orifices those as explained in US 4.813.653 are used.
- an equally distributed carrying gas stream is created in the upward direction, whereby the bed is fluidized, and the carrying gas that emerges at the top is then evacuated from the fluidized bed chamber via outlet opening 12.
- the outlet temperature is regulated to about 420°C, and this corresponds to a heat drain of about 12 KW.
- This comparatively low portion, taken by the primary cooling by the carrying gas (less than 15 KW per m bed surface,), of the total cooling capacity is possible in this quenching step of the patenting operation, because the largest portion of the heat is removed via the depoty cooling.
- the procury cooling occurs by means of air, that is sucked from the surrounding athmosphere by a ventilator 22 via inlet 36, and that is further blown, via flow regulator 23, through a system of pipes 24 towards an outlet 25.
- the pipe system consists in this case of eight pipes 26 having an U-form, that are immersed in oblique position in the bed, and that are connected together in parallel.
- the plane of each U, and also both legs of the U are perpendicular to the plane of the drawing, so that the U-form can not be seen.
- the U-form can be seen, although it is not located in the (horizontal) plane of the drawing.
- Each one of the eight U's comprises a straight and horizontally running entrance leg 27 and exit leg 28, that are connected together into a U-form by means of an elbow 29. All entrance legs 27 lie in the same horizontal plane 30 (Figure 1), and all exit legs 28 in another subjacent plane 31.
- the diameter of the pipes is not so large, and the pipe system not so compact, as to prevent to look through the pipe system in vertical projection ( Figure 2). Between the different legs, an interspace 32 is always visible in vertical projection. In this way, the fluidization through this comparatively compact pipe system is not jeopardized.
- cooling elements be not concentrated in a single horizontal plane, but that they should rather be distributed over two or more horizontal planes. It has further to be seen that the interspaces between the cooling elements can be reached as well as possible by the vertical gas stream, and that the resistance against this stream be distributed as equally as possible over the bed surface.
- the entrance and exit legs 27 respectively 28, are connected in parallel to an entrance and exit tube, 33 respectively 34, via a number of vertically running connecting tubes 35 outside the casing.
- the entrance and exit legs mustnot necessarily be perpendicular to the traveling direction of the wires, but may cross that direction otherwise than perpendicularly, although the perpendicular crossing is preferred.
- the flow regulator 23 is steered by a control system 37 for the control of the temperature of the fluidized bed around the wires, in order to keep this temperature at a constant value, despite all disturbances, such as fluctuations of the heat drain by the carrying gas, or of the heat input via the wire (mainly speed changes).
- a regulating system comprises a feeling device (not shown) of the temperature, located in the fluidized bed in the proximity of the wires, and that sends its output signal to a comparator that measures the deviation of the measured value from the desired value. This deviation is then transformed, in an analog or digital way, into a correction signal (having, as usual, a proportional, differential and integral portion), and this correction signal acts on flow regulator 23 so as to increase or to reduce the cooling air flow to the extent as wanted.
- a correction signal having, as usual, a proportional, differential and integral portion
- the cooling pipes are made of steel and have an outer diameter of 4.8 cm. This gives a cooling surface of about 2 m per square meter of bed surface. In normal operation with wires of 2 mm diameter traveling through the bed at 0,475 m/sec, the exit temperature of the air is then about 200°C at a nominal flow of 2000 Nm3 per hour, and this corresponds to a nominal heat-drain of about 93 KW, taking into account the heating-up of the air in the sucking ventilator. This is a heat drain capacity of 7.75 times the heat drain capacity of the primary cooling system.
- the advantage of the invention can however sufficiently be exploited when the cooling surface of the depoty circuit is larger than 0.4 m per square meter of bed surface and when the heat drain by the furnishy circuit is larger than three times the heat drain of the primary circuit.
- the second, third and fourth fluidized bed chamber respectively 4 to 6, have each, in this example of embodiment, an own inlet for the carrying gas.
- the carrying gas shall be blown in at this temperature (between 530°C and 570°C). This temperature can be different from one chamber to the other.
- This carrying gas shall preferably come from the same austenitizing furnace, but has to be cooled down to a lesser extent.
- the invention is not limited to quenching in the patenting operation, but can be applied in any installation with one or more fluidized bed chambers, in which each chamber has its own function in an overall heat treatment programme that the steel wires have to undergo, and in which one of these chambers serve for quenching from a higher temperature to a lower one, which has however not to be below about 250°C, in order to avoid condensation of moistness in the carrying gas.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Heat Treatment Of Strip Materials And Filament Materials (AREA)
Claims (13)
- Einrichtung, die zum kontinuierlichen Abschrecken von Stahldrähten auf eine Temperatur von unterstenfalls 250°C geeignet ist und eine Wirbelbett-Kühlkammer (3) aufweist, welche mit einem indirekten Konvektionskühler (24) versehen ist, dadurch gekennzeichnet, daß die Einrichtung eine Luftquelle (23) aufweist, welche mit einem Einlaß (33) des Konvektionskühlers verbunden ist, daß der Konvektionskühler eine Kühlfläche von wenigstens 0.4 m pro Quadratmeter Wirbelbettfläche aufweist, daß der spezifische Wärmestrom H (H = Luftstrom x spezifische Wärme) der Luftströmung durch den Konvektionskühler variabel ist und daß der Konvektionskühler ferner ein Reguliersystem (37) aufweist. um durch Änderung des spezifischen Wärmestroms die Wirbelbetttemperatur auf einem konstanten Wert zu halten.
- Einrichtung nach Anspruch 1, dadurch gekennzeichnet, daß der Ausgangsstrom der Luftquelle (23) variabel ist und durch das Ausgangssignal des Regulierers (37) gesteuert ist.
- Einrichtung nach einem der Ansprüche 1 oder 2, dadurch gekennzeichnet, daß der Einlaß (33) des Konvektionskühlers einen Flüssigkeitszerstäuber umfaßt, welcher dazu ausgeführt ist, einen Flüssigkeitssprühnebel in den Durchgang der Luftströmung von der Luftquelle zum Konvektionskühler einzuspritzen, welcher Zerstäuber einen variablen Ausgangsstrom aufweist und durch das Ausgangssignal des Regulierers (37) gesteuert ist.
- Einrichtung nach einem der Ansprüche 1 bis 3, dadurch gekennzeichnet, daß der Konvektionskühler (24) eine Anzahl von Kühlelementen (26) umfaßt, welche über mehr als eine Horizontalebene (30, 31) verteilt sind, wobei die Vertikalprojektion der Kühlelemente einer Ebene die Vertikalprojektion der Elemente einer anderen Ebene nicht überdeckt und wobei die Vertikalprojektion aller Kühlelemente nur maximal 80 % der gesamten Bettfläche einnimmt.
- Einrichtung nach Anspruch 4. dadurch gekennzeichnet, daß der Konvektionskühler (24) eine Anzahl von Kühlrohren (26) in U-Form umfaßt, deren Schenkel (27. 28) horizontal durch das Bett (13) in einer Richtung quer zur Axialrichtung der Drähte (1) verlaufen, wobei die Rohre mit einem Schenkel (27) in einer oberen (30) und mit dem anderen Schenkel (28) in einer unteren (31) Horizontalebene liegen und in Vertikalprojektion Zwischenräume (32) zwischen den Schenkeln aufweisen und wobei die Schenkel zwischen dem Einlaß (33) und dem Auslaß (25) des Konvektionskühlers parallel geschaltet sind.
- Einrichtung nach einem der vorhergehenden Ansprüche. dadurch gekennzeichnet, daß sie mit einem umgebenden Gehäuse (9) ausgeführt ist, welches die Atmosphäre in und oberhalb des Wirbelbetts von der Außenatmosphäre trennt und dessen Einlaß (11) für das Traggas über eine Kühlvorrichtung (18) mit dem Abgasauslaß eines Ofens verbunden ist.
- Einrichtung, die zum kontinuierlichen Patentieren einer Reihe von Stahldrähten geeignet ist, welche Seite an Seite parallel zueinander und in Axialrichtung der Drähte laufen, und einen Ofen zur Austenitisierung der Drähte gefolgt von einer Wirbelbetteinrichtung zur Abschreckung und sorbitischen Umwandl ung der Drähte umfaßt, wobei die Wirbelbetteinrichtung eine Anzahl benachbarter Wirbelbettkammern (3, 4, 5, 6) umfaßt, welche unmittelbar aufeinanderfolgen, dadurch gekennzeichnet, daß die erste Kammer (3) als Einrichtung nach einem der Ansprüche 1 bis 6 ausgeführt ist.
- Verfahren zum kontinuierlichen Abschrecken von Stahldrähten (1) auf eine Temperatur von unterstenfalls 250°C, bei dem die Drähte kontinuierlich durch ein Wirbelbett (13) geführt werden, welches einen Tauchkonvektionskühler (24) umfaßt, dadurch gekennzeichnet, daß eine Luftströmung durch den Konvektionskühler geschickt wird und hierbei wenigstens dreimal die durch das Traggas des Wirbelbetts abgeführte Wärme entzogen wird und daß die Temperatur des Wirbelbetts durch Steuerung des spezifischen Wärmestroms H der Kühlluft auf einen konstanten Wert reguliert wird.
- Verfahren nach Anspruch 8. dadurch gekennzeichnet, daß die Temperatur des Wirbelbetts durch Änderung des durch den Konvektionskühler geschickten Luftstroms reguliert wird.
- Verfahren nach einem der Ansprüche 8 oder 9, dadurch gekennzeichnet, daß eine zerstäubte Flüssigkeit in den Luftstrom eingespritzt wird und die Temperatur des Wirbelbetts durch Änderung der Menge der eingespritzen zerstäubten Flüssigkeit reguliert wird.
- Verfahren nach einem der Ansprüche 8 bis 10, dadurch gekennzeichnet, daß das Wirbelbett unter einer nicht oxidierenden Atmosphäre gehalten wird und das Traggas für das Wirbelbett von einer Verbrennungsvorrichtung geliefert wird, in der eine Verbrennung unter Verringerung des Sauerstoffs durchgeführt wird.
- Verfahren zum kontinuierlichen Patentieren von Stahldrähten (1), welche zunächst durch einen Austenitisierungsofen geführt werden und dann in einem Wirbelbett (13) abgeschreckt werden, wobei die Drähte eine sorbitische Umwandlung durchlaufen. dadurch gekennzeichnet, daß zum Abschrecken das Verfahren nach einem der Ansprüche 8 bis 11 angewendet wird und daß das Traggas den Abgasen des Austenitisierungsofens entnommen wird.
- Verfahren nach Anspruch 12, dadurch gekennzeichnet, daß das Traggas eine Wärme von nicht mehr als 15 KW pro m Bettfläche und der Konvektionskühler wenigstens 50 KW pro m entziehen.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| BE8900809 | 1989-07-26 | ||
| BE8900809A BE1004383A3 (nl) | 1989-07-26 | 1989-07-26 | Wervelbed voor het afschrikken van staaldraad. |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0410501A1 EP0410501A1 (de) | 1991-01-30 |
| EP0410501B1 true EP0410501B1 (de) | 1996-01-17 |
Family
ID=3884263
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP90201864A Expired - Lifetime EP0410501B1 (de) | 1989-07-26 | 1990-07-10 | Wirbelbett zum Abschrecken von Stahldrähten |
Country Status (7)
| Country | Link |
|---|---|
| EP (1) | EP0410501B1 (de) |
| JP (1) | JP2931053B2 (de) |
| KR (1) | KR0180725B1 (de) |
| BE (1) | BE1004383A3 (de) |
| BR (1) | BR9003605A (de) |
| DE (1) | DE69024869T2 (de) |
| ES (1) | ES2084648T3 (de) |
Families Citing this family (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FI20011954A7 (fi) * | 2001-10-08 | 2003-04-09 | Lahden Laempoekaesittely Oy | Lämpökäsittelymenetelmä |
| JP3968406B1 (ja) * | 2006-08-16 | 2007-08-29 | 株式会社アルケミー | 鋼線材のパテンティング方法 |
| ES2667468T3 (es) | 2008-04-30 | 2018-05-11 | Nv Bekaert Sa | Filamento de acero patentado en bismuto |
| WO2019239184A1 (en) | 2018-06-13 | 2019-12-19 | Arcelormittal | Vacuum deposition facility and method for coating a substrate |
| WO2019239186A1 (en) | 2018-06-13 | 2019-12-19 | Arcelormittal | Vacuum deposition facility and method for coating a substrate |
| JP2020143344A (ja) * | 2019-03-07 | 2020-09-10 | 山田 榮子 | 鋼線の加熱冷却用流動床炉 |
| KR102204335B1 (ko) | 2020-08-31 | 2021-01-18 | 소병현 | 이동식 교반기능을 갖는 퇴비용 부숙 건조기 |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1490853A (fr) * | 1966-08-25 | 1967-08-04 | Schloemann Ag | Dispositif pour le patentage continu de fil laminé |
| DE1602081B1 (de) * | 1967-03-04 | 1970-05-27 | Huettenwerk Oberhausen Ag | Vorrichtung fuer die Waermebehandlung von metallischem Gut,insbesondere Walzdraht |
| US3718024A (en) * | 1971-02-12 | 1973-02-27 | Morgan Construction Co | Apparatus including a fluidized bed for cooling steel rod through transformation |
| DE3226582A1 (de) * | 1982-07-16 | 1984-01-19 | Ewald Schwing Verfahrenstechnik GmbH, 4133 Neukirchen-Vluyn | Vorrichtung zum kuehlen von stabmaterial |
| GB8426455D0 (en) * | 1984-10-19 | 1984-11-28 | Bekaert Sa Nv | Fluidised bed apparatus |
| GB8505491D0 (en) * | 1985-03-04 | 1985-04-03 | Bekaert Sa Nv | Heat treatment of steel |
| DE3734169A1 (de) * | 1987-10-09 | 1989-04-27 | Ewald Schwing | Verfahren zum warmbadhaerten von gegenstaenden aus legierten staehlen |
-
1989
- 1989-07-26 BE BE8900809A patent/BE1004383A3/nl not_active IP Right Cessation
-
1990
- 1990-07-10 EP EP90201864A patent/EP0410501B1/de not_active Expired - Lifetime
- 1990-07-10 ES ES90201864T patent/ES2084648T3/es not_active Expired - Fee Related
- 1990-07-10 DE DE69024869T patent/DE69024869T2/de not_active Expired - Fee Related
- 1990-07-25 BR BR909003605A patent/BR9003605A/pt not_active Application Discontinuation
- 1990-07-26 JP JP2198950A patent/JP2931053B2/ja not_active Expired - Lifetime
- 1990-07-26 KR KR1019900011387A patent/KR0180725B1/ko not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| KR0180725B1 (ko) | 1999-02-18 |
| DE69024869T2 (de) | 1996-05-30 |
| EP0410501A1 (de) | 1991-01-30 |
| KR910003120A (ko) | 1991-02-26 |
| DE69024869D1 (de) | 1996-02-29 |
| BR9003605A (pt) | 1991-08-27 |
| JPH03146623A (ja) | 1991-06-21 |
| ES2084648T3 (es) | 1996-05-16 |
| BE1004383A3 (nl) | 1992-11-10 |
| JP2931053B2 (ja) | 1999-08-09 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA1195946A (en) | Coking method and a device for performing the same | |
| NL1005541C2 (nl) | Werkwijze voor het koelen van een oven alsmede oven voorzien van een koelinrichting. | |
| US3677234A (en) | Heating apparatus and process | |
| US5145534A (en) | Fluidized bed for quenching steel wire and process thereof | |
| US6962676B1 (en) | Method and apparatus in a fluidized bed heat exchanger | |
| EP0410501A1 (de) | Wirbelbett zum Abschrecken von Stahldrähten | |
| WO1994011672A1 (en) | Method and apparatus for recovering heat in a fluidized bed reactor | |
| US4423856A (en) | Controlled cooling apparatus for hot rolled wire rods | |
| US3820955A (en) | Horizontal high severity furnace | |
| US5441547A (en) | Method for gasification of a finely divided combustible material | |
| US20090136884A1 (en) | Direct-Fired Furnace Utilizing An Inert Gas To Protect Products Being Thermally Treated In The Furnace | |
| US5803937A (en) | Method of cooling a dust-laden raw gas from the gasification of a solid carbon-containing fuel | |
| CA1081158A (en) | Method of and an arrangement for preheating coking coal | |
| US5595001A (en) | Apparatus for producing sodium perborate monohydrate and product produced thereby | |
| EP0722999B1 (de) | Vorrichtung zum Kühlen von mit Feststoffen beladenen Gasen | |
| EP0128734B1 (de) | Verfahren zum Abkühlen von Stahlband in einem Durchlaufglühofen | |
| KR890003701B1 (ko) | 유동상 반응 장치 및 그 제어 방법 | |
| CA2021383A1 (en) | Fluidized bed for quenching steel wires | |
| US4725321A (en) | Method for cooling a steel strip in a continuous annealing furnace | |
| US4883115A (en) | Method and apparatus for cooling high-temperature processes | |
| US3262685A (en) | Gas quencher | |
| US4724014A (en) | Method for cooling a steel strip in a continuous annealing furnace | |
| US5772969A (en) | Method and apparatus for recovering heat in a fluidized bed reactor | |
| US5660148A (en) | Method and device in the cooling of the circulating material in a fluidized-bed boiler | |
| US2902982A (en) | Forced circulation vapor generating units |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): BE DE DK ES FR GB GR IT LU NL |
|
| 17P | Request for examination filed |
Effective date: 19910228 |
|
| 17Q | First examination report despatched |
Effective date: 19921214 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): BE DE DK ES FR GB GR IT LU NL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19960117 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19960117 Ref country code: DK Effective date: 19960117 Ref country code: BE Effective date: 19960117 |
|
| REF | Corresponds to: |
Ref document number: 69024869 Country of ref document: DE Date of ref document: 19960229 |
|
| ET | Fr: translation filed | ||
| ITF | It: translation for a ep patent filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2084648 Country of ref document: ES Kind code of ref document: T3 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19960611 Year of fee payment: 7 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 19960709 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19960731 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: THE PATENT HAS BEEN ANNULLED BY A DECISION OF A NATIONAL AUTHORITY Effective date: 19970711 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980331 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20001204 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20010615 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20010616 Year of fee payment: 12 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020710 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030201 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20020710 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050710 |