EP0446499A1 - Procédé pour abaisser la vitesse d'étirage de machines d'étirage à tambours - Google Patents
Procédé pour abaisser la vitesse d'étirage de machines d'étirage à tambours Download PDFInfo
- Publication number
- EP0446499A1 EP0446499A1 EP90250071A EP90250071A EP0446499A1 EP 0446499 A1 EP0446499 A1 EP 0446499A1 EP 90250071 A EP90250071 A EP 90250071A EP 90250071 A EP90250071 A EP 90250071A EP 0446499 A1 EP0446499 A1 EP 0446499A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- train
- tube
- length
- pipe
- speed
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C1/00—Manufacture of metal sheets, wire, rods, tubes or like semi-manufactured products by drawing
- B21C1/02—Drawing metal wire or like flexible metallic material by drawing machines or apparatus in which the drawing action is effected by drums
- B21C1/12—Regulating or controlling speed of drawing drums, e.g. to influence tension; Drives; Stop or relief mechanisms
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21C—MANUFACTURE OF METAL SHEETS, WIRE, RODS, TUBES, PROFILES OR LIKE SEMI-MANUFACTURED PRODUCTS OTHERWISE THAN BY ROLLING; AUXILIARY OPERATIONS USED IN CONNECTION WITH METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL
- B21C1/00—Manufacture of metal sheets, wire, rods, tubes or like semi-manufactured products by drawing
- B21C1/02—Drawing metal wire or like flexible metallic material by drawing machines or apparatus in which the drawing action is effected by drums
Definitions
- the invention relates to a method for automatically lowering the drawing speed of drum drawing machines for pipes or the like before the drawing end of a tube bundle, each of a plurality of tube bundles drawn in succession after a pull through the drawing tool being collected in a receiving basket, which in each case gradually after the tube bundle has been drawn into a discharge station is transported, from where another of several pulling processes that are carried out in the same order is initiated.
- a container Arranged below the drawing drum is a container which is referred to as a receiving basket and is dimensioned such that the largest possible weights of the bobbins can be taken up in one length even with the smallest drawn tube dimensions.
- Pipes are reduced in several passes, for example based on the dimensions 55 x 2.5 mm and a unit weight of 300 kg to 6 x 0.35 mm.
- the pipes are 5,450 m long.
- the pick-up basket with a full length of pipe is transported from its position below the drawing drum to the discharge station, from where the pipe end is fed as the new pipe start to the next train of the drawing drum, while a new free pick-up basket is brought below the drawing drum into the pick-up station .
- several, about six to seven, baskets are on the way and are fed to the drawing drum one after the other.
- the pulling speed must be reduced, on the one hand so that the last tube turns do not swing back and forth in the drain basket uncontrollably and the pipe end would whip out of the basket and on the other hand so that the relief shock that arises when the pipe end leaves the drawing ring and the drawing force collapses, is greatly reduced.
- the maximum achievable drawing speed is currently 1,200 m / min. A reduction of this drawing speed at the end of the train to approx. 60 m / min. is imperative.
- Another known method proposes to mark several turns of the tube behind the drawing ring by means of paint spraying. On the next train, this mark is recognized by sensors and used as a signal to reduce the speed of the drawing drum drive. This method takes advantage of the fact that the beginning of the pipe falling into the receiving basket becomes the end of the pipe on the next train. This method has so far not been successful in practice because there are no suitable marking colors on the market that guarantee the optical identification of the pipe end section.
- the present invention has for its object to develop a method and an apparatus for automatically lowering the drawing speed of drum drawing machines, which can be easily activated by the operator on the first move of each drawing game and then for the other moves of this draw game are no longer changed.
- the method therefore suggests recording the pipe lengths during the first draws of all the pipe bundles and comparing them with the extension of the first pipe bundle after the second train.
- the constants Q and D that can be calculated from this are used to determine the switchover points for the following pipes of this draft game, without having to intervene again by hand.
- the corresponding device works, for example, with pulse counters. After storing all lengths (impulses) of all (usually seven bundles of pipes), the operator observes the basket when pulling the first bundle of pipes of the second train and switches manually to low speed when there are only a few turns in the basket. The impulses are counted and recorded from the start of drawing to the switchover point. In addition, the impulses from the start of drawing to the end of drawing this tube are counted and registered. The quotient Q from the counted pulses from the start of drawing to the end of drawing this drawn tube and the counted pulses to the end of drawing of the tube drawn in the first train is a measure of the extension of the pipe in the second train. The current diameter of the drawing ring and stopper are also taken into account, which also influence the length of the finished pipe.
- the pulses counted until the switch to low speed are subtracted from the number of pulses that result between the start of pull and the end of pull of the second train.
- the difference D formed in this way represents a measure of the pipe length which has to be driven at a reduced drawing speed.
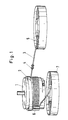
- the drawing shows the principle of a continuous drum drawing machine on which the method according to the invention can be carried out.
- the tube turns, as indicated at 2 are wound in several revolutions in a known manner.
- a frictional force is thereby achieved which makes it possible to pull the tube 3 through the drawing tool 4 and thereby reduce it.
- the pipe windings to be drawn lie in the drain basket 5 of the drain station (not shown in more detail), while the reduced, drawn pipe windings are thrown off by the drawing drum 1 into the receiving basket 7 arranged underneath. This is done in that the subsequent pipe coils 2 press the coils already on the drawing drum downwards so that they fall down when they come out of the area of the pressure roller 6.
- the receiving basket 7 As soon as the receiving basket 7 is filled with a complete tube length of, for example, 5,000 m, the receiving basket 7 is brought into the drain station and is there to the drain basket 5. The end of a drawn tube winding is introduced as the beginning of a new tube to be drawn in the next train in the continuous drum drawing machine, so that a second and further trains can be carried out in the same way.
- a measuring device on the drum drawing machine emits a pulse per m tube. With a pipe length of 200 m after the first train, 200 pulses would then be stored.
- the operator has switched the machine to slow speed after 250 m or 250 pulses, i. H. the 36 pulses to the end of the drawing correspond to the tube length of 36 m, which are driven at reduced speed.
- the machine would accordingly have to be switched to slow drawing speed after 393 pulses corresponding to 393 m.
- the number of pulses is counted from the start of the pull to the end of the pull and saved; this value serves as the basis for the calculation for the next drawing game.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Metal Extraction Processes (AREA)
Priority Applications (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE90250071T DE59003554D1 (de) | 1990-03-15 | 1990-03-15 | Verfahren zur Absenkung der Ziehgeschwindigkeit von Trommelziehmaschinen. |
| EP90250071A EP0446499B1 (fr) | 1990-03-15 | 1990-03-15 | Procédé pour abaisser la vitesse d'étirage de machines d'étirage à tambours |
| US07/500,041 US5014531A (en) | 1990-03-15 | 1990-03-27 | Method for automatically reducing the drawing speed of a tubular material drawing machine |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP90250071A EP0446499B1 (fr) | 1990-03-15 | 1990-03-15 | Procédé pour abaisser la vitesse d'étirage de machines d'étirage à tambours |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0446499A1 true EP0446499A1 (fr) | 1991-09-18 |
| EP0446499B1 EP0446499B1 (fr) | 1993-11-18 |
Family
ID=8205225
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP90250071A Expired - Lifetime EP0446499B1 (fr) | 1990-03-15 | 1990-03-15 | Procédé pour abaisser la vitesse d'étirage de machines d'étirage à tambours |
Country Status (3)
| Country | Link |
|---|---|
| US (1) | US5014531A (fr) |
| EP (1) | EP0446499B1 (fr) |
| DE (1) | DE59003554D1 (fr) |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2057909A (en) * | 1935-05-18 | 1936-10-20 | Cutler Hammer Inc | Motor controller |
| US3337154A (en) * | 1966-02-16 | 1967-08-22 | Westinghouse Electric Corp | Motor control system for coiling apparatus |
| GB1151523A (en) * | 1965-09-20 | 1969-05-07 | Marshall Richards Machine Comp | Improvements in and relating to Tube Drawing Machines |
| GB2126509A (en) * | 1982-09-03 | 1984-03-28 | Mannesmann Ag | Drum drawing machine |
| DE3708859C1 (de) * | 1987-03-17 | 1988-06-01 | Mannesmann Ag | Verfahren und Vorrichtung zur Durchfuehrung des Verfahrens zur automatischen Drehzahlsteuerung einer Konti-Trommelziehmaschine fuer Rohre oder dergleichen |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3539085A (en) * | 1968-06-11 | 1970-11-10 | Web Press Eng Inc | Web control system |
| US3593558A (en) * | 1969-07-24 | 1971-07-20 | Fenn Mfg Co The | Payoff reel controller |
| DE2132408C3 (de) * | 1971-06-30 | 1982-03-11 | Benteler-Werke Ag Werk Neuhaus, 4790 Paderborn | Anordnung zur Beeinflussung der Drehzahl der Elektromotoren der Einzelantriebe einer Mehrfachziehanlage |
| DE3725511C1 (fr) * | 1987-07-29 | 1988-03-10 | Mannesmann Ag, 4000 Duesseldorf, De |
-
1990
- 1990-03-15 EP EP90250071A patent/EP0446499B1/fr not_active Expired - Lifetime
- 1990-03-15 DE DE90250071T patent/DE59003554D1/de not_active Expired - Fee Related
- 1990-03-27 US US07/500,041 patent/US5014531A/en not_active Expired - Fee Related
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2057909A (en) * | 1935-05-18 | 1936-10-20 | Cutler Hammer Inc | Motor controller |
| GB1151523A (en) * | 1965-09-20 | 1969-05-07 | Marshall Richards Machine Comp | Improvements in and relating to Tube Drawing Machines |
| US3337154A (en) * | 1966-02-16 | 1967-08-22 | Westinghouse Electric Corp | Motor control system for coiling apparatus |
| GB2126509A (en) * | 1982-09-03 | 1984-03-28 | Mannesmann Ag | Drum drawing machine |
| DE3708859C1 (de) * | 1987-03-17 | 1988-06-01 | Mannesmann Ag | Verfahren und Vorrichtung zur Durchfuehrung des Verfahrens zur automatischen Drehzahlsteuerung einer Konti-Trommelziehmaschine fuer Rohre oder dergleichen |
Also Published As
| Publication number | Publication date |
|---|---|
| US5014531A (en) | 1991-05-14 |
| DE59003554D1 (de) | 1993-12-23 |
| EP0446499B1 (fr) | 1993-11-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3809635C2 (fr) | ||
| DE3833958C2 (de) | Vorrichtung zum Aufspulen von drahtförmigem Gut auf zweiflanschige Spulen | |
| EP0017613B1 (fr) | Procédé pour déterminer une valeur proportionnelle à la longueur d'un fil dévidé axialement d'une bobine de filature ou d'un bobine à fil croisé et dispositifs pour réaliser ce procédé | |
| DE3708859C1 (de) | Verfahren und Vorrichtung zur Durchfuehrung des Verfahrens zur automatischen Drehzahlsteuerung einer Konti-Trommelziehmaschine fuer Rohre oder dergleichen | |
| EP0446499B1 (fr) | Procédé pour abaisser la vitesse d'étirage de machines d'étirage à tambours | |
| DE69414645T2 (de) | Verbessertes Spulenwickelverfahren und Spulmaschinen zu dessen Durchführung | |
| DE3030504C2 (de) | Verfahren und Vorrichtung zur Erzeugung von Garnspulen mit vorgegebener Garnlänge auf Rotorspinnmaschinen | |
| DE2165525C2 (de) | Bandwickelmaschine | |
| DE2640312C2 (de) | Vorrichtung zum Einleiten eines automatischen Auflaufspulenwechsels | |
| DE3445678A1 (de) | Vorrichtung zum konstanthalten der anzahl der zwischen einer spinnmaschine und einer spulmaschine in einem kreislauf befindlichen spulenhuelsen | |
| DE976938C (de) | Drahthaspel mit ortsfester Wickelstelle | |
| DE4119833C1 (fr) | ||
| EP0099959A1 (fr) | Dispositif pour ranger des bobines de fil | |
| CH676837A5 (fr) | ||
| DE19523937B4 (de) | Verfahren und Vorrichtung zum Topfspinnen | |
| DE1710127A1 (de) | Verfahren zur UEberwachung der Spulstellen einer automatischen Spulmaschine | |
| DE3504883A1 (de) | Verfahren und vorrichtung zum beschicken eines spulautomaten mit kopsen | |
| DE3604018A1 (de) | Verfahren und vorrichtung zum herstellen von kreuzspulenpaaren | |
| DE1932549C3 (de) | Vorrichtung zum Überwachen des Fertigungsprozesses einer automatischen Spulmaschine | |
| DE1760457B2 (de) | Vorrichtung an einer doppeldrahtzwirnmaschine zum bestuecken der spulenaufnehmer mit lieferspulen | |
| DE2614252B2 (de) | Verfahren zur Herstellung einer Fadenreserve | |
| EP1123996B1 (fr) | Méthode pour séparer automatiquement la mèche pendant l'enlèvement dans un banc à broches | |
| DE2344600A1 (de) | Verfahren zur erhoehung der massengleichmaessigkeit von garn beim offen-endspinnvorgang und vorrichtung zum durchfuehren dieses verfahrens | |
| DE612948C (de) | Vickelvorrichtung fuer Watte | |
| DE183018C (fr) |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE GB IT |
|
| 17P | Request for examination filed |
Effective date: 19911217 |
|
| 17Q | First examination report despatched |
Effective date: 19920708 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE GB IT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRE;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED.SCRIBED TIME-LIMIT Effective date: 19931118 |
|
| REF | Corresponds to: |
Ref document number: 59003554 Country of ref document: DE Date of ref document: 19931223 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19940215 Year of fee payment: 5 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19940218 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19940526 Year of fee payment: 5 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19950315 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19950315 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19951201 |