EP0521396A1 - Méthode et dispositif pour enrouler et couper transversalement une bande - Google Patents
Méthode et dispositif pour enrouler et couper transversalement une bande Download PDFInfo
- Publication number
- EP0521396A1 EP0521396A1 EP92110751A EP92110751A EP0521396A1 EP 0521396 A1 EP0521396 A1 EP 0521396A1 EP 92110751 A EP92110751 A EP 92110751A EP 92110751 A EP92110751 A EP 92110751A EP 0521396 A1 EP0521396 A1 EP 0521396A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- winding
- contact roller
- material web
- web
- tube
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000004804 winding Methods 0.000 title claims abstract description 62
- 238000000034 method Methods 0.000 title claims abstract description 11
- 239000000463 material Substances 0.000 claims abstract description 22
- 238000005520 cutting process Methods 0.000 claims description 12
- 238000000926 separation method Methods 0.000 claims description 5
- 230000008878 coupling Effects 0.000 claims description 2
- 238000010168 coupling process Methods 0.000 claims description 2
- 238000005859 coupling reaction Methods 0.000 claims description 2
- 230000000977 initiatory effect Effects 0.000 claims 1
- 238000006073 displacement reaction Methods 0.000 abstract 1
- 239000011248 coating agent Substances 0.000 description 3
- 238000000576 coating method Methods 0.000 description 3
- 230000005540 biological transmission Effects 0.000 description 1
- 238000006243 chemical reaction Methods 0.000 description 1
- 239000003292 glue Substances 0.000 description 1
- 238000011835 investigation Methods 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 229920003023 plastic Polymers 0.000 description 1
- 239000002985 plastic film Substances 0.000 description 1
- -1 polyethylene terephthalate Polymers 0.000 description 1
- 229920000139 polyethylene terephthalate Polymers 0.000 description 1
- 239000005020 polyethylene terephthalate Substances 0.000 description 1
- 230000006641 stabilisation Effects 0.000 description 1
- 238000011105 stabilization Methods 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H19/00—Changing the web roll
- B65H19/22—Changing the web roll in winding mechanisms or in connection with winding operations
- B65H19/2207—Changing the web roll in winding mechanisms or in connection with winding operations the web roll being driven by a winding mechanism of the centre or core drive type
- B65H19/2215—Turret-type with two roll supports
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2408/00—Specific machines
- B65H2408/20—Specific machines for handling web(s)
- B65H2408/23—Winding machines
- B65H2408/231—Turret winders
- B65H2408/2313—Turret winders with plurality of reel supporting or back-up rollers travelling around turret axis
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2408/00—Specific machines
- B65H2408/20—Specific machines for handling web(s)
- B65H2408/23—Winding machines
- B65H2408/231—Turret winders
- B65H2408/2315—Turret winders specified by number of arms
- B65H2408/23152—Turret winders specified by number of arms with two arms
Definitions
- the invention relates to a device and a method for winding and cross-cutting a running material web, which is wound on a winding tube until a certain winding diameter is reached, wherein a contact roller presses the material web against the winding tube and before an unwinded winding tube into the Conversion position is transferred, a cutting member cuts the web of material between the wound and the still unwound winding tube perpendicular to the direction of travel.
- the material web can be, for example, a paper web, a film web or one with a web magnetic coating provided plastic sheet.
- the task is to separate the material web wound on a winding tube with a separating knife after reaching a certain winding diameter and to wind the new material web beginning that has been formed onto an empty winding tube while the full package is being removed and replaced by an empty winding tube.
- the almost completely wound winding tube leaves its winding position.
- a new sleeve to be wound takes its place.
- the running web is cut between the new and wound winding tube and lies against the new tube, whereupon the process just mentioned begins again.
- the finished wrap runs out in order to be removed. It has been shown that especially the outermost winding layer package often shifts or is axially displaceable relative to the rest of the winding, especially with smooth material webs and at high machine speeds in the range of 300 m / min. This telescoping of the winding, that is to say deviations from the winding with the same edge, can damage parts of the winding by deformation.
- the invention had for its object to achieve a stabilization of the winding pattern when braking the full winding reel to a standstill, the run-out time of the reel should also be reduced in order to achieve a quick reel change in a turret winder.
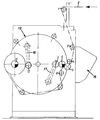
- a material web (2) coming from a coating device (not shown) runs over deflection rollers (1, 3, 4) to the winding and cross-cutting device.
- a contact roller (5) places the material web (2) on the winding (6).
- a second contact roller (7) which is rotatably mounted on an arm (17), stabilizes the winding.
- An identical one Device, namely contact roller (12) and arm (16) is provided in an analogous manner for the winding core (11) to be rewound.
- the entire device (18) is turned so that the sketched state is reached. Then the material web between the empty winding tube (6) and the deflecting roller (8) is separated by a cross cutting device (15), and the newly formed beginning of the web is placed against the winding tube (6). The full roll wound on the winding tube (11) is then braked from the outside to a standstill by the braked contact roller. The contact roller remains pressed against the reel for a selected period of time until it is pivoted against an empty winding tube in order to change the filled reel. The winder remains in this position until the winding core (6) is almost filled and the described turning process begins again.
- each of the winding tubes is designed to be drivable and brakable and that the contact rollers (7, 12) present in addition to the usual contact roller, as in the German application 41 07 127 already mentioned, can be braked.
- the contact roller (12) acting on the full winding is braked with a braking torque which is suitable for preventing the winding from telescoping.
- the size of the braking torque to be selected depends on the moment of inertia of the winding and the torque always acting on the winding tube, which results from the bearing friction of the tube bearing, the friction in the drive motor and the transmission gear.
- an approximately 70 cm wide plastic web consisting of 15 ⁇ thick polyethylene terephthalate, which was provided with a 3 ⁇ m thick magnetic coating, was used at a speed of 500 m / min. wound up.
- the above-mentioned web which had a length of 10,000 m, could be brought to a standstill within 5 seconds without the outermost winding layers being blurred.
- the winding behavior was excellent, the web also showed on the outer layers after the deduction. There are no scratches or damage to the glue point or the end and beginning of the web.
Landscapes
- Replacement Of Web Rolls (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE4121944 | 1991-07-03 | ||
| DE4121944A DE4121944A1 (de) | 1991-07-03 | 1991-07-03 | Vorrichtung und verfahren zum aufwickeln und querschneiden einer laufenden materialbahn |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0521396A1 true EP0521396A1 (fr) | 1993-01-07 |
| EP0521396B1 EP0521396B1 (fr) | 1995-09-13 |
Family
ID=6435296
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP92110751A Expired - Lifetime EP0521396B1 (fr) | 1991-07-03 | 1992-06-25 | Méthode et dispositif pour enrouler et couper transversalement une bande |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP0521396B1 (fr) |
| DE (2) | DE4121944A1 (fr) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2007107940A1 (fr) * | 2006-03-17 | 2007-09-27 | The Procter & Gamble Company | Procédé de rebobinage d'un matériau en bande |
| WO2008043748A1 (fr) * | 2006-10-09 | 2008-04-17 | Windmöller & Hölscher Kg | Rouleau presseur pivotant dans une bobineuse à retournement |
| WO2009050556A1 (fr) * | 2007-10-18 | 2009-04-23 | Colines S.P.A. | Système d'enroulement destiné à être utilisé dans des lignes de production de films plastiques, en particulier de films plastiques extensibles, et procédé pour enrouler les films plastiques sur des bobines |
| US7559503B2 (en) | 2006-03-17 | 2009-07-14 | The Procter & Gamble Company | Apparatus for rewinding web materials |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4431140A (en) * | 1981-11-27 | 1984-02-14 | The Black Clawson Company | Continuous pressure roll winder |
| GB2126564A (en) * | 1982-09-13 | 1984-03-28 | Worldwide Converting Mach | Turret winder |
| EP0167715A1 (fr) * | 1984-07-11 | 1986-01-15 | SMG Stahlkontor Maschinenbau GmbH | Dispositif de changement de rouleaux pour mandrins à diamètres différents |
| EP0394197A2 (fr) * | 1989-04-21 | 1990-10-24 | Gottlieb Looser | Procédé et dispositif d'enroulement |
| US4993652A (en) * | 1989-11-06 | 1991-02-19 | The Black Clawson Company | Continuous winder for web materials |
-
1991
- 1991-07-03 DE DE4121944A patent/DE4121944A1/de not_active Withdrawn
-
1992
- 1992-06-25 EP EP92110751A patent/EP0521396B1/fr not_active Expired - Lifetime
- 1992-06-25 DE DE59203646T patent/DE59203646D1/de not_active Expired - Fee Related
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4431140A (en) * | 1981-11-27 | 1984-02-14 | The Black Clawson Company | Continuous pressure roll winder |
| GB2126564A (en) * | 1982-09-13 | 1984-03-28 | Worldwide Converting Mach | Turret winder |
| EP0167715A1 (fr) * | 1984-07-11 | 1986-01-15 | SMG Stahlkontor Maschinenbau GmbH | Dispositif de changement de rouleaux pour mandrins à diamètres différents |
| EP0394197A2 (fr) * | 1989-04-21 | 1990-10-24 | Gottlieb Looser | Procédé et dispositif d'enroulement |
| US4993652A (en) * | 1989-11-06 | 1991-02-19 | The Black Clawson Company | Continuous winder for web materials |
Cited By (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2007107940A1 (fr) * | 2006-03-17 | 2007-09-27 | The Procter & Gamble Company | Procédé de rebobinage d'un matériau en bande |
| US7559503B2 (en) | 2006-03-17 | 2009-07-14 | The Procter & Gamble Company | Apparatus for rewinding web materials |
| US8459586B2 (en) | 2006-03-17 | 2013-06-11 | The Procter & Gamble Company | Process for rewinding a web material |
| WO2008043748A1 (fr) * | 2006-10-09 | 2008-04-17 | Windmöller & Hölscher Kg | Rouleau presseur pivotant dans une bobineuse à retournement |
| CN101553422B (zh) * | 2006-10-09 | 2012-03-28 | 温德莫勒及霍尔希尔公司 | 回转卷绕机中的可摆动的定位辊 |
| US8201768B2 (en) | 2006-10-09 | 2012-06-19 | Windmoeller & Hoelscher Kg | Pivotable positioning roller in the reversing winder |
| WO2009050556A1 (fr) * | 2007-10-18 | 2009-04-23 | Colines S.P.A. | Système d'enroulement destiné à être utilisé dans des lignes de production de films plastiques, en particulier de films plastiques extensibles, et procédé pour enrouler les films plastiques sur des bobines |
| CN101827769B (zh) * | 2007-10-18 | 2012-07-25 | 科林斯股份公司 | 用于塑料膜生产线中尤其是可延伸塑料膜的卷绕系统以及用于卷绕塑料膜卷的方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0521396B1 (fr) | 1995-09-13 |
| DE4121944A1 (de) | 1993-01-07 |
| DE59203646D1 (de) | 1995-10-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE2361343C2 (fr) | ||
| DE4141242C2 (fr) | ||
| DE69420793T2 (de) | Vorrichtung zum Wickeln | |
| EP0450312A1 (fr) | Procédé pour épisser le début d'une bande enroulée avec la fin d'une autre bande enroulée. | |
| DE4033900A1 (de) | Splice-stelle und verfahren zum herstellen einer splice-stelle am bahnanfang eines bahnwickels | |
| EP0442038A2 (fr) | Méthode et dispositif pour le remplacement automatique d'une bobine pleine par un nouveau noyau d'enroulement | |
| DE69414702T2 (de) | Mechanismus und verfahren zum überleiten einer materialbahn für einen stetigwickler | |
| DE3030798A1 (de) | Verfahren und vorrichtung zum laengsschneiden und aufwickeln von bahnfoermigem material | |
| DE4336298A1 (de) | Abwickelvorrichtung mit einer Spliceeinrichtung | |
| DE2600522A1 (de) | Wickelmaschine | |
| AT402056B (de) | Wickelmaschine | |
| EP1897830B1 (fr) | Dispositif destiné à lier une première bande de matériau à une deuxième bande de matériau | |
| EP0521396B1 (fr) | Méthode et dispositif pour enrouler et couper transversalement une bande | |
| DE2303856A1 (de) | Vorrichtung zur verbindung zweier baender insbesondere fuer aufgespulte produkte | |
| EP0352564A2 (fr) | Procédé et dispositif de manipulation et de traitement ultérieur d'une bande du type en nid d'abeilles | |
| DE2344870C3 (de) | Vorrichtung zur endweisen Verbindung zweier Bahnen | |
| EP0963909B1 (fr) | Procédé et dispositif pour fabriquer un rouleau de matériau en bande emballée circonférenciellement, et un rouleau de matériau en bande | |
| AT413377B (de) | Verfahren für einen wickelwechsel in einer wickelstation und band zur verwendung in dem verfahren | |
| AT511278B1 (de) | Verfahren in zusammenhang mit einer rollenschneidmaschine für eine faserbahn | |
| EP1295830B2 (fr) | Echangeur de rouleaux et méthode pour le changement automatique de rouleaux pendat l'arrêt | |
| EP0503363A1 (fr) | Dispositif de coupe et d'application de bandes dans une machine à enrouler | |
| DE4222880C2 (de) | Splicevorrichtung | |
| EP1621497A1 (fr) | Méthode et dispositif pour la préparation d'un rouleau de bande de papier en stockage pour le changement du rouleau en marche | |
| DE19652448C9 (de) | Vorrichtung zum Verpacken einer Materialbahnrolle mit einer Verpackungsbahn | |
| DE19652448C1 (de) | Vorrichtung zum Verpacken einer Materialbahnrolle mit einer Verpackungsbahn |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19921021 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE FR GB |
|
| 17Q | First examination report despatched |
Effective date: 19940808 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB |
|
| REF | Corresponds to: |
Ref document number: 59203646 Country of ref document: DE Date of ref document: 19951019 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19951002 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: TP Ref country code: FR Ref legal event code: CD Ref country code: FR Ref legal event code: CA |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: TP Free format text: CORRECTION Ref country code: FR Ref legal event code: CD Free format text: CORRECTION Ref country code: FR Ref legal event code: CA Free format text: CORRECTION |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20020603 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20020605 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20020611 Year of fee payment: 11 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030625 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040101 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20030625 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040227 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |