EP0532331A1 - Revêtement coulé sur place à base de fer - Google Patents
Revêtement coulé sur place à base de fer Download PDFInfo
- Publication number
- EP0532331A1 EP0532331A1 EP92308259A EP92308259A EP0532331A1 EP 0532331 A1 EP0532331 A1 EP 0532331A1 EP 92308259 A EP92308259 A EP 92308259A EP 92308259 A EP92308259 A EP 92308259A EP 0532331 A1 EP0532331 A1 EP 0532331A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- aluminium
- grooves
- liner
- sleeve
- low pressure
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D19/00—Casting in, on, or around objects which form part of the product
- B22D19/0009—Cylinders, pistons
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D19/00—Casting in, on, or around objects which form part of the product
- B22D19/0081—Casting in, on, or around objects which form part of the product pretreatment of the insert, e.g. for enhancing the bonding between insert and surrounding cast metal
Definitions
- This invention relates to cast-in-place iron based liners and a method of casting an aluminium cylinder block having such liners
- Metallurgical bonding although it is not thoroughly understood, has proved unsuccessful possibly because the lighter weight metal, such as aluminium, has a strong tendency to chill and form an oxide film at the interface in at least some minor zone.
- complex castings such as aluminium engine blocks having intricately-shaped water jackets and a number of thin- walled cylinder walls, the ability to keep the aluminium at a sufficiently high temperature, at 100% of the interface with a liner, is extremely difficult. As the aluminium fully solidifies, it moves away (shrinks) and thus delaminates in at least such minor zone. As a result, there is a degraded heat transfer characteristic for the block that prevents such technique from being used commercially. At best, there is only 80-85% lay-up of the aluminium along the iron-based liner interface wall.
- the interfacing surface of the casting iron liners has been roughened by spiny protrusions when such liners are initially formed by casting; such protrusions act as longitudinal and circumferential mechanical bonds when aluminium is cast under high pressure (die-cast) therearound.
- High pressure is always required to move the aluminium across such protrusions and still achieve lay-up of aluminium against the original outer wall of the liner.
- the machined smooth wall of the liner becomes the valleys between the protrusions. Because of the need for quick high pressure mould filling to prevent premature freezing, such technique is impractical when casting aluminium engine blocks by low pressure (in the range of 2-5 psi), and mould filling times take an average of one-half minute.
- the invention is a cast-in-place liner construction useful in low pressure casting of hollow aluminium parts, the construction is characterised by an iron-based cylindrical body having a surface thereof imprinted with a repeating pattern of crossed groups of relief grooves, each groove forming a helix along such surface, the spacing between such grooves and the depth of such grooves being uniformly controlled to permit the grooves to act as molten aluminium runners during low pressure casting of the aluminium that facilitates laying-up of the aluminium along the entire surface.
- the grooves advantageously will have a depth in the range of .02-.04 inch; the spacing between grooves is advantageously .20-.30 inch; and a width for each of such grooves in the range of .02-.04 inch.
- the included angle between intersecting groups of grooves is in the range of 35-55°.
- the imprinted surface is the outer cylindrical surface of the liner while the inner cylindrical surface thereof is smooth.
- a second aspect of this invention is a casting method deploying such liner, the method comprising: (a) imprinting a cylindrical surface of a sleeve that is designed to interface with cast aluminium thereagainst, the imprinting providing a quilted pattern of shallow grooves, such grooves being sized and spaced to promote transfer of molten aluminium during low pressure filling of the mould containing such sleeve; and (b) planting the liner in such mould and introducing aluminium thereagainst at a low pressure to form a desired aluminium casting.
- the imprinting may be carried out by machining the prefabricated sleeve or by imprinting indentations in the sleeve during rolling or fabrication of such sleeve.
- Casting in place of iron cylinder liners in an aluminium cylinder block is considered routine when the block is produced by high pressure die casting. Molten metal is injected under high pressure and for a short period of time to facilitate the lay-up of the aluminium against the iron liner. However, for casting processes such as gravity or low pressure where mould filling occurs over a relatively long period and takes place with little or no pressure, the casting-in-place of liners is considered extremely difficult.
- This invention provides for a unique quilted pattern of grooving on the surface of the iron liner that is to interface with the aluminium, such pattern promoting the flow of molten aluminium against the iron cylinder bore liner surface to overcome the problem of chilling and accompanying oxide formation.
- the iron-based liner 20 has a cylindrical body B provided with an outer surface 10 and an inner cylindrical surface 11, and a pattern C imprinted onto the outer cylindrical surface 10, which pattern is comprised of crossed groups 12 and 13 of relief grooves 14.
- the grooves are effective to uniformly act as molten aluminium runners during low pressure casting to facilitate laying-up of the aluminium along the entire cylindrical surface 10.
- the grooves create a diamond-shaped pattern as criss-crossed, the lateral spacing 15 between adjacent grooves being on the order of .20-.30 inch, the depth 16 of each of the grooves being in the range of .02-.04 inch, and the width 17 of each of the grooves being desirably in the range of .02-.04 inches.
- the included angle 18 between intersecting or crossing grooves is in the range of 35-55°.
- the pattern is imprinted on the outer cylindrical surface by either machining such pattern as the sleeve is rotated, or the pattern may be formed by indentations in the liner during rolling or casting of the liner itself.
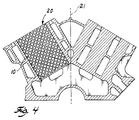
- the grooves in each of the groups are helical about the outer surface of the liner; this is advantageous when placing the liner in an oblique position such as shown in Figure 4 for a V-shaped configuration aluminium block. In such application, one set of grooves will be somewhat horizontal with respect to a vertical plane 21 and the other set of grooves will be closer to the vertical plane as they wrap around the outer surface of the liner.
- a casting method deploying such liners comprises: (a) imprinting a cylindrical surface of a iron-based sleeve designed to interface with a cast aluminium thereagainst, the sleeve having a quilted pattern of shallow grooves with the grooves sized and spaced to promote transfer of molten aluminium during a low pressure filling of a mould containing the sleeve; and (b) planting the liner in such mould and introducing aluminium thereagainst at a low pressure to form the desired aluminium casting.
- the pressure employed in such method is in the range of 2-5 psi and the temperature of the molten aluminium will be in the range of 1275°F. Due to the pattern of the grooves and their critical sizing, the molten aluminium will not drop below a fluid temperature during filling of the mould and will not prematurely freeze in migrating throughout all of the interstices of the cylindrical surface of the liner.
- the grooves are defined to have a depth in excess of .04 inch, there will be a tendency for the aluminium to freeze or form a miniscus characteristic of problems associated with the prior art. If the depth of the grooves is less than .02, there is little likelihood that a molten aluminium runner effect will be created. If groove spacing is greater than .3 inch, the ability to lay aluminium throughout the normal cylindrical surface is hindered, whereas a spacing between grooves of less than .20 inch will create difficulty in filling all the grooves with molten aluminium because of the lack of pressure driving the aluminium through such an increased maze of grooves. The ultimate effect of this invention achieves essentially 100% lay-up of aluminium against the iron- based liner after the completion of the low pressure casting technique. By “lay-up” it is herein meant: the amount of intimate contact between the outer surface of the iron liner and the aluminium barrel that surrounds the liner.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Cylinder Crankcases Of Internal Combustion Engines (AREA)
- Pistons, Piston Rings, And Cylinders (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US75813191A | 1991-09-12 | 1991-09-12 | |
| US758131 | 1991-09-12 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0532331A1 true EP0532331A1 (fr) | 1993-03-17 |
| EP0532331B1 EP0532331B1 (fr) | 1996-12-18 |
Family
ID=25050625
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19920308259 Expired - Lifetime EP0532331B1 (fr) | 1991-09-12 | 1992-09-10 | Revêtement coulé sur place à base de fer |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0532331B1 (fr) |
| CA (1) | CA2077187A1 (fr) |
| DE (1) | DE69216018T2 (fr) |
| MX (1) | MX9204697A (fr) |
Cited By (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0826444A1 (fr) * | 1996-08-27 | 1998-03-04 | Daimler-Benz Aktiengesellschaft | Ebauche en métal léger utilisé comme pièce d'insertion dans un autre objet en métal léger et procédé de traitement de surface de cette ébauche |
| WO1999043457A1 (fr) * | 1998-02-25 | 1999-09-02 | Daimlerchrysler Ag | Procede pour produire une ebauche de chemise de cylindre, a couler dans le carter en alliage leger d'un moteur a piston alternatif |
| EP1002602A1 (fr) * | 1998-11-21 | 2000-05-24 | VAW alucast GmbH | Dispositif et procédé pour la fabrication d'un bloc moteur |
| EP1110644A1 (fr) * | 1999-12-15 | 2001-06-27 | Teipi Industry Co., Ltd. | Insert coulé à rugosité controlée pour moulage avec insert et produit fabriqué par ce procédé de moulage |
| DE10012787A1 (de) * | 2000-03-16 | 2001-09-20 | Volkswagen Ag | Verfahren zur Herstellung von Leichtmetallgussteilen mit eingegossenen Buchsen und Buchse zum Eingiessen |
| EP1504833A4 (fr) * | 2002-05-13 | 2005-07-20 | Honda Motor Co Ltd | Coquille interne de moulage de fonte et procede de production de celle-ci |
| US7172011B2 (en) | 2001-05-25 | 2007-02-06 | Mahle Gmbh | Method for the production of a lost-foam casting model for a light metal cylinder liner |
| WO2011131712A1 (fr) * | 2010-04-23 | 2011-10-27 | Rheinisch-Westfälische Technische Hochschule Aachen | Pièce coulée composite hybride métallique |
| US20160252042A1 (en) * | 2015-02-27 | 2016-09-01 | Avl Powertrain Engineering, Inc. | Cylinder Liner |
| US11499499B1 (en) | 2021-10-05 | 2022-11-15 | Brunswick Corporation | Marine engines, cylinder liners for marine engines, and methods and assemblies for forming marine engines |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102017214732A1 (de) * | 2017-08-23 | 2019-02-28 | Bayerische Motoren Werke Aktiengesellschaft | Verfahren zur Auslegung eines Bauteil- oder Werkstoffverbunds |
| DE102018122407A1 (de) * | 2018-09-13 | 2020-03-19 | Bergmann Automotive GmbH | Zylinderlaufbuchse für einen Kolbenmotor |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR450434A (fr) * | 1912-11-11 | 1913-03-25 | Anthelme Girel | Procédé de fabrication de cylindres de moteurs, en acier avec chemise de fonte brasée |
| GB873012A (en) * | 1959-01-02 | 1961-07-19 | Aluminum Co Of America | Cast bimetallic articles |
| US3069209A (en) * | 1958-07-16 | 1962-12-18 | Alfred F Bauer | Method of bonding a bi-metallic casting |
| US3401026A (en) * | 1966-01-19 | 1968-09-10 | Gen Motors Corp | Method of forming a bimetallic article |
| EP0491978A1 (fr) * | 1989-12-15 | 1992-07-01 | Audi Ag | Bloc cylindre pour moteur à explosion |
-
1992
- 1992-08-13 MX MX9204697A patent/MX9204697A/es unknown
- 1992-08-28 CA CA 2077187 patent/CA2077187A1/fr not_active Abandoned
- 1992-09-10 EP EP19920308259 patent/EP0532331B1/fr not_active Expired - Lifetime
- 1992-09-10 DE DE1992616018 patent/DE69216018T2/de not_active Expired - Lifetime
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR450434A (fr) * | 1912-11-11 | 1913-03-25 | Anthelme Girel | Procédé de fabrication de cylindres de moteurs, en acier avec chemise de fonte brasée |
| US3069209A (en) * | 1958-07-16 | 1962-12-18 | Alfred F Bauer | Method of bonding a bi-metallic casting |
| GB873012A (en) * | 1959-01-02 | 1961-07-19 | Aluminum Co Of America | Cast bimetallic articles |
| US3401026A (en) * | 1966-01-19 | 1968-09-10 | Gen Motors Corp | Method of forming a bimetallic article |
| EP0491978A1 (fr) * | 1989-12-15 | 1992-07-01 | Audi Ag | Bloc cylindre pour moteur à explosion |
Cited By (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6074763A (en) * | 1996-08-27 | 2000-06-13 | Daimlerchrysler Ag | Light metal part activation for casting with another light metal part |
| EP0826444A1 (fr) * | 1996-08-27 | 1998-03-04 | Daimler-Benz Aktiengesellschaft | Ebauche en métal léger utilisé comme pièce d'insertion dans un autre objet en métal léger et procédé de traitement de surface de cette ébauche |
| US6286583B1 (en) | 1996-08-27 | 2001-09-11 | Daimlerchrysler Ag | Two part light metal coating and method of making same |
| US6286210B1 (en) | 1998-02-25 | 2001-09-11 | Daimlerchrysler Ag | Method for producing a cylinder liner blank to be cast into a light-alloy crankcase of a reciprocating engine |
| WO1999043457A1 (fr) * | 1998-02-25 | 1999-09-02 | Daimlerchrysler Ag | Procede pour produire une ebauche de chemise de cylindre, a couler dans le carter en alliage leger d'un moteur a piston alternatif |
| EP1002602A1 (fr) * | 1998-11-21 | 2000-05-24 | VAW alucast GmbH | Dispositif et procédé pour la fabrication d'un bloc moteur |
| EP1110644A1 (fr) * | 1999-12-15 | 2001-06-27 | Teipi Industry Co., Ltd. | Insert coulé à rugosité controlée pour moulage avec insert et produit fabriqué par ce procédé de moulage |
| DE10012787A1 (de) * | 2000-03-16 | 2001-09-20 | Volkswagen Ag | Verfahren zur Herstellung von Leichtmetallgussteilen mit eingegossenen Buchsen und Buchse zum Eingiessen |
| DE10012787B4 (de) * | 2000-03-16 | 2008-04-10 | Volkswagen Ag | Verfahren zur Herstellung von Leichtmetallgussteilen mit eingegossenen Buchsen |
| US7172011B2 (en) | 2001-05-25 | 2007-02-06 | Mahle Gmbh | Method for the production of a lost-foam casting model for a light metal cylinder liner |
| EP1504833A4 (fr) * | 2002-05-13 | 2005-07-20 | Honda Motor Co Ltd | Coquille interne de moulage de fonte et procede de production de celle-ci |
| US7226667B2 (en) | 2002-05-13 | 2007-06-05 | Honda Giken Kogyo Kabushiki Kaisha | Cast-iron insert and method of manufacturing same |
| WO2011131712A1 (fr) * | 2010-04-23 | 2011-10-27 | Rheinisch-Westfälische Technische Hochschule Aachen | Pièce coulée composite hybride métallique |
| US20160252042A1 (en) * | 2015-02-27 | 2016-09-01 | Avl Powertrain Engineering, Inc. | Cylinder Liner |
| US11499499B1 (en) | 2021-10-05 | 2022-11-15 | Brunswick Corporation | Marine engines, cylinder liners for marine engines, and methods and assemblies for forming marine engines |
Also Published As
| Publication number | Publication date |
|---|---|
| DE69216018D1 (de) | 1997-01-30 |
| CA2077187A1 (fr) | 1993-03-13 |
| EP0532331B1 (fr) | 1996-12-18 |
| MX9204697A (es) | 1993-03-01 |
| DE69216018T2 (de) | 1997-04-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0532331B1 (fr) | Revêtement coulé sur place à base de fer | |
| DE69025288T2 (de) | Vollformgiessen eines Motorblockes aus zwei Legierungen | |
| CA1186482A (fr) | Methode de production d'un bloc moteur en aluminium coule | |
| US4865112A (en) | Method of casting metals with integral heat exchange piping | |
| EP1002602B1 (fr) | Dispositif et procédé pour la fabrication d'un bloc moteur | |
| DE69216512T2 (de) | Verfahren und Vorrichtung zum Giessen in Giessformen aus Graphit | |
| US2244367A (en) | Making composite metal articles | |
| US5676192A (en) | Cast-in process | |
| EP0565503B1 (fr) | Procédé et moule pour la production de chemises de cylindre en fonte | |
| US4491168A (en) | Wear resistant insert for cast lightweighted pistons and method of casting | |
| DE4100779C2 (fr) | ||
| PL287149A1 (en) | Method of making a cylinder for top-poured continuous casting mould and cylinder made thereby | |
| SU1586854A1 (ru) | Металлическа форма дл центробежного лить валков | |
| RU2084307C1 (ru) | Обогреваемая прибыль | |
| RU2177859C2 (ru) | Способ изготовления литых полых металлических изделий | |
| JPH09168855A (ja) | 樹脂成形用金型の製造方法および装置 | |
| JPS558321A (en) | Repair method of steel ingot casting mold and molding board | |
| JPS59110451A (ja) | 鋼の連続鋳造装置 | |
| JPH05285509A (ja) | 圧延用複合ロールの製造方法 | |
| DE3441569A1 (de) | Verfahren zur herstellung von verbundgusskoerpern nach dem schleudergiessverfahren | |
| JPS6199539A (ja) | 非鉄クラツド鋳塊およびその製造方法 | |
| SU806240A1 (ru) | Способ центробежного лить биметал-личЕСКиХ чЕРВ чНыХ КОлЕС | |
| JPH01284459A (ja) | クラッド鋼材の製造装置 | |
| JPS6411925A (en) | Method for preventing cracking of austenitic stainless steel or high-alloy steel at the time of rapid solidification | |
| JPH0234248A (ja) | 鋳造金型に冷却水路管を形成させる方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE FR GB IT |
|
| 17P | Request for examination filed |
Effective date: 19930821 |
|
| 17Q | First examination report despatched |
Effective date: 19950703 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB IT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 19961218 Ref country code: FR Effective date: 19961218 |
|
| REF | Corresponds to: |
Ref document number: 69216018 Country of ref document: DE Date of ref document: 19970130 |
|
| EN | Fr: translation not filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19970827 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19970904 Year of fee payment: 6 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 746 Effective date: 19970815 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF THE APPLICANT RENOUNCES Effective date: 19980901 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980910 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19980910 |