EP0532806B1 - Une vis dure en acier austénitique inoxydable et procédé de sa fabrication - Google Patents
Une vis dure en acier austénitique inoxydable et procédé de sa fabrication Download PDFInfo
- Publication number
- EP0532806B1 EP0532806B1 EP91308660A EP91308660A EP0532806B1 EP 0532806 B1 EP0532806 B1 EP 0532806B1 EP 91308660 A EP91308660 A EP 91308660A EP 91308660 A EP91308660 A EP 91308660A EP 0532806 B1 EP0532806 B1 EP 0532806B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- screw
- stainless steel
- austenitic stainless
- layer
- nitrided
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 229910000963 austenitic stainless steel Inorganic materials 0.000 title claims abstract description 44
- 238000000034 method Methods 0.000 title claims abstract description 19
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 6
- 238000005121 nitriding Methods 0.000 claims description 22
- KRHYYFGTRYWZRS-UHFFFAOYSA-M Fluoride anion Chemical compound [F-] KRHYYFGTRYWZRS-UHFFFAOYSA-M 0.000 claims description 13
- 239000002253 acid Substances 0.000 claims description 13
- 229910001220 stainless steel Inorganic materials 0.000 claims description 6
- 239000010935 stainless steel Substances 0.000 claims description 6
- 238000010438 heat treatment Methods 0.000 claims description 4
- 239000010410 layer Substances 0.000 description 85
- 239000007789 gas Substances 0.000 description 23
- 238000005553 drilling Methods 0.000 description 19
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 description 18
- 238000005260 corrosion Methods 0.000 description 13
- 238000010079 rubber tapping Methods 0.000 description 13
- QGZKDVFQNNGYKY-UHFFFAOYSA-N Ammonia Chemical compound N QGZKDVFQNNGYKY-UHFFFAOYSA-N 0.000 description 12
- 230000007797 corrosion Effects 0.000 description 12
- JEIPFZHSYJVQDO-UHFFFAOYSA-N iron(III) oxide Inorganic materials O=[Fe]O[Fe]=O JEIPFZHSYJVQDO-UHFFFAOYSA-N 0.000 description 12
- GRYLNZFGIOXLOG-UHFFFAOYSA-N Nitric acid Chemical compound O[N+]([O-])=O GRYLNZFGIOXLOG-UHFFFAOYSA-N 0.000 description 8
- 229910045601 alloy Inorganic materials 0.000 description 8
- 239000000956 alloy Substances 0.000 description 8
- 229910052742 iron Inorganic materials 0.000 description 8
- 229910017604 nitric acid Inorganic materials 0.000 description 8
- 239000000243 solution Substances 0.000 description 8
- 229910000831 Steel Inorganic materials 0.000 description 6
- 239000011248 coating agent Substances 0.000 description 6
- 150000003839 salts Chemical class 0.000 description 6
- 239000010959 steel Substances 0.000 description 6
- 238000000576 coating method Methods 0.000 description 5
- 238000007598 dipping method Methods 0.000 description 5
- 239000011737 fluorine Substances 0.000 description 5
- 229910052731 fluorine Inorganic materials 0.000 description 5
- 229910052751 metal Inorganic materials 0.000 description 5
- 239000002184 metal Substances 0.000 description 5
- 229910000069 nitrogen hydride Inorganic materials 0.000 description 5
- YCKRFDGAMUMZLT-UHFFFAOYSA-N Fluorine atom Chemical compound [F] YCKRFDGAMUMZLT-UHFFFAOYSA-N 0.000 description 4
- UQSXHKLRYXJYBZ-UHFFFAOYSA-N Iron oxide Chemical compound [Fe]=O UQSXHKLRYXJYBZ-UHFFFAOYSA-N 0.000 description 4
- 239000011651 chromium Substances 0.000 description 4
- 230000006866 deterioration Effects 0.000 description 4
- QDOXWKRWXJOMAK-UHFFFAOYSA-N dichromium trioxide Chemical compound O=[Cr]O[Cr]=O QDOXWKRWXJOMAK-UHFFFAOYSA-N 0.000 description 4
- 229920005989 resin Polymers 0.000 description 4
- 239000011347 resin Substances 0.000 description 4
- 239000007921 spray Substances 0.000 description 4
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 4
- 229910000975 Carbon steel Inorganic materials 0.000 description 3
- 238000003916 acid precipitation Methods 0.000 description 3
- 229910052799 carbon Inorganic materials 0.000 description 3
- 239000010962 carbon steel Substances 0.000 description 3
- 238000006243 chemical reaction Methods 0.000 description 3
- 238000005516 engineering process Methods 0.000 description 3
- 239000007788 liquid Substances 0.000 description 3
- 239000000463 material Substances 0.000 description 3
- 238000007747 plating Methods 0.000 description 3
- 239000000126 substance Substances 0.000 description 3
- 239000002344 surface layer Substances 0.000 description 3
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 description 2
- 229910021565 Chromium(IV) fluoride Inorganic materials 0.000 description 2
- 229910019912 CrN Inorganic materials 0.000 description 2
- BZHJMEDXRYGGRV-UHFFFAOYSA-N Vinyl chloride Chemical compound ClC=C BZHJMEDXRYGGRV-UHFFFAOYSA-N 0.000 description 2
- 230000015572 biosynthetic process Effects 0.000 description 2
- 150000001875 compounds Chemical class 0.000 description 2
- 230000006378 damage Effects 0.000 description 2
- SZVJSHCCFOBDDC-UHFFFAOYSA-N ferrosoferric oxide Chemical compound O=[Fe]O[Fe]O[Fe]=O SZVJSHCCFOBDDC-UHFFFAOYSA-N 0.000 description 2
- 239000011261 inert gas Substances 0.000 description 2
- FZGIHSNZYGFUGM-UHFFFAOYSA-L iron(ii) fluoride Chemical compound [F-].[F-].[Fe+2] FZGIHSNZYGFUGM-UHFFFAOYSA-L 0.000 description 2
- 230000000873 masking effect Effects 0.000 description 2
- 229920005990 polystyrene resin Polymers 0.000 description 2
- 230000002265 prevention Effects 0.000 description 2
- 239000012495 reaction gas Substances 0.000 description 2
- 238000009991 scouring Methods 0.000 description 2
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 description 1
- 229910021562 Chromium(II) fluoride Inorganic materials 0.000 description 1
- 229910000705 Fe2N Inorganic materials 0.000 description 1
- 229910017389 Fe3N Inorganic materials 0.000 description 1
- 229910000727 Fe4N Inorganic materials 0.000 description 1
- XPDWGBQVDMORPB-UHFFFAOYSA-N Fluoroform Chemical compound FC(F)F XPDWGBQVDMORPB-UHFFFAOYSA-N 0.000 description 1
- 241000221535 Pucciniales Species 0.000 description 1
- 229910004014 SiF4 Inorganic materials 0.000 description 1
- XSTXAVWGXDQKEL-UHFFFAOYSA-N Trichloroethylene Chemical group ClC=C(Cl)Cl XSTXAVWGXDQKEL-UHFFFAOYSA-N 0.000 description 1
- HCHKCACWOHOZIP-UHFFFAOYSA-N Zinc Chemical compound [Zn] HCHKCACWOHOZIP-UHFFFAOYSA-N 0.000 description 1
- 238000010521 absorption reaction Methods 0.000 description 1
- 230000001133 acceleration Effects 0.000 description 1
- 238000010306 acid treatment Methods 0.000 description 1
- 229910021529 ammonia Inorganic materials 0.000 description 1
- 230000008901 benefit Effects 0.000 description 1
- 238000005256 carbonitriding Methods 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 229910052804 chromium Inorganic materials 0.000 description 1
- RNFYGEKNFJULJY-UHFFFAOYSA-L chromium(ii) fluoride Chemical compound [F-].[F-].[Cr+2] RNFYGEKNFJULJY-UHFFFAOYSA-L 0.000 description 1
- 239000000356 contaminant Substances 0.000 description 1
- 230000003247 decreasing effect Effects 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- RWRIWBAIICGTTQ-UHFFFAOYSA-N difluoromethane Chemical compound FCF RWRIWBAIICGTTQ-UHFFFAOYSA-N 0.000 description 1
- 239000012895 dilution Substances 0.000 description 1
- 238000010790 dilution Methods 0.000 description 1
- 230000007613 environmental effect Effects 0.000 description 1
- 150000002221 fluorine Chemical class 0.000 description 1
- NBVXSUQYWXRMNV-UHFFFAOYSA-N fluoromethane Chemical compound FC NBVXSUQYWXRMNV-UHFFFAOYSA-N 0.000 description 1
- -1 for example Substances 0.000 description 1
- WMIYKQLTONQJES-UHFFFAOYSA-N hexafluoroethane Chemical compound FC(F)(F)C(F)(F)F WMIYKQLTONQJES-UHFFFAOYSA-N 0.000 description 1
- 229910000765 intermetallic Inorganic materials 0.000 description 1
- SHXXPRJOPFJRHA-UHFFFAOYSA-K iron(iii) fluoride Chemical compound F[Fe](F)F SHXXPRJOPFJRHA-UHFFFAOYSA-K 0.000 description 1
- 238000010297 mechanical methods and process Methods 0.000 description 1
- 239000000203 mixture Substances 0.000 description 1
- 230000007935 neutral effect Effects 0.000 description 1
- 150000004767 nitrides Chemical class 0.000 description 1
- 125000004433 nitrogen atom Chemical group N* 0.000 description 1
- 230000001473 noxious effect Effects 0.000 description 1
- 230000003647 oxidation Effects 0.000 description 1
- 238000007254 oxidation reaction Methods 0.000 description 1
- 238000010422 painting Methods 0.000 description 1
- 230000008569 process Effects 0.000 description 1
- 230000009257 reactivity Effects 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- ABTOQLMXBSRXSM-UHFFFAOYSA-N silicon tetrafluoride Chemical compound F[Si](F)(F)F ABTOQLMXBSRXSM-UHFFFAOYSA-N 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
- 239000006104 solid solution Substances 0.000 description 1
- 241000894007 species Species 0.000 description 1
- UBOXGVDOUJQMTN-UHFFFAOYSA-N trichloroethylene Natural products ClCC(Cl)Cl UBOXGVDOUJQMTN-UHFFFAOYSA-N 0.000 description 1
- NXHILIPIEUBEPD-UHFFFAOYSA-H tungsten hexafluoride Chemical compound F[W](F)(F)(F)(F)F NXHILIPIEUBEPD-UHFFFAOYSA-H 0.000 description 1
- 125000000391 vinyl group Chemical group [H]C([*])=C([H])[H] 0.000 description 1
- 229920002554 vinyl polymer Polymers 0.000 description 1
- 239000011701 zinc Substances 0.000 description 1
- 229910052725 zinc Inorganic materials 0.000 description 1
Images

Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C8/00—Solid state diffusion of only non-metal elements into metallic material surfaces; Chemical surface treatment of metallic material by reaction of the surface with a reactive gas, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals
- C23C8/06—Solid state diffusion of only non-metal elements into metallic material surfaces; Chemical surface treatment of metallic material by reaction of the surface with a reactive gas, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals using gases
- C23C8/08—Solid state diffusion of only non-metal elements into metallic material surfaces; Chemical surface treatment of metallic material by reaction of the surface with a reactive gas, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals using gases only one element being applied
- C23C8/24—Nitriding
- C23C8/26—Nitriding of ferrous surfaces
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C8/00—Solid state diffusion of only non-metal elements into metallic material surfaces; Chemical surface treatment of metallic material by reaction of the surface with a reactive gas, leaving reaction products of surface material in the coating, e.g. conversion coatings, passivation of metals
- C23C8/80—After-treatment
Definitions
- This invention relates to a method for manufacturing a a hard austenitic stainless steel article, for example a screw or bolt, which has excellent corrosion resistance.
- an austenitic stainless steel is higher in corrosion resistance against acid or salt compared than a carbon steel.
- it is inferior to carbon steel. Therefore, it has not been proper to use austenitic stainless steel for a screw which particularly needs to be able to tighten to an iron-based plate by self-tapping, such as a tapping screw, a self-drilling screw or a dry wall screw.
- plated carburized iron articles or 13 Cr stainless steel articles are used.
- these articles are not only inferior in oxidation resistance (rust resistance) to austenitic stainless steel articles but are also weak in their tightening function because of corrosion of their base material by acid rain, which is a major environmental problem of today.
- Austenitic stainless steel articles are far superior in acid resistance. Accordingly, the present inventors provided new technology for maintaining the tapping property as well as carburized iron articles by nitriding-hardening the austenitic stainless steel screw (Japanese Patent Application No. 177660/1989).
- a nitrided hard layer with which even a thick iron plate can be drilled and tapped self-forcedly is formed over the entire surface of the austenitic stainless steel screw.
- this new technology has a serious defect in that the so formed nitrided hard layer lacks the corrosion resistance characteristic of austenitic stainless steel.
- the screw head exposed to the atmosphere, readily rusts.
- its head and the neighbourhood of the head are visible, and are exposed to the atmosphere.
- An austenitic stainless steel screw is devalued as commercial goods by even a bit of change in the color of its head because of rust. It is possible to conduct plating or color-painting on the surface of a nitrided hard layer after nitriding in order to prevent rust from being generated there. However, this is only a temporary solution, not a fundamental one. So as to protect the screw head or the like against nitriding, it was proposed to apply some methods, such as copper-plating and a masking by flame coating, to these parts prior to nitriding. Even if such methods are employed, it is difficult to completely prevent nitriding on the surface of the portion of the austenitic stainless steel base.
- FR 2 404 142 discloses a method of forming a nitrided layer over only part of a corrosion-resistant steel screw comprising forming a substantially gas-impervious metallic layer on the part of the screw which is not to be hardened, which metallic layer may be removed after the hardening treatment.
- the invention provides a method for manufacturing a hard austenitic stainless steel article comprising forming a nitrided hard layer on the surface of an austentic stainless steel article and removing the nitrided hard layer from predetermined parts of the nitrided article to expose unnitrided stainless steel.
- a nitrided hard layer of the austenitic stainless steel screw has a thickness of 30 to 200 »m in general, preferably 40 to 80 »m for improving tapping and drilling functions.
- Sixty to seventy percent of the thickness of the nitrided hard layer comprises an alloy layer (surface layer) including a large amount of intermetallic compounds such as CrN and Fe x N y , and a diffused layer (inner layer) of a solid solution of N and C.
- the alloy layer formed on the very surface of the nitrided hard layer suffers from severe deterioration in corrosion resistance due to a considerable decrease in concentration of solid soluble Cr.
- an inner diffused layer is superior to the alloy layer in corrosion resistance, but not sufficiently good compared with a pure austenitic stainless base of the core portion.
- nitrided hard layer by nitriding, it takes 4 to 8 hours for the surface of the nitrided hard layer to rust in a neutral salt spray test, 500 to 700 hours for a diffused layer after removing the alloy layer from the nitrided hard layer to rust, and over 2000 hours for a pure austenitic base per se exposed by removal of the entire thickness of the nitrided layer to rust.
- This means that corrosion resistance can be improved without deterioration in the tapping and drilling properties, which were strengthened by nitriding, when the nitrided hard layer is removed from the screw head and the like, exposed to the atmosphere in a tightened state.
- the nitrided layer formed on the screw head, a neck portion, and the like of the screw which are in contact with the atmosphere when tightened is removed.
- Austenitic stainless steel base is exposed where the nitrided layer is removed to achieve rust prevention and corrosion resistance characteristic of austenitic stainless steel per se .
- the nitrided hard layer formed over the entire surface of the austenitic stainless steel screw comprises an alloy layer, which is a surface layer, and a diffused layer, which is an inner layer, as mentioned above.
- the alloy layer has a thickness of 15 to 50»m and a surface hardness (Hv) of 750 to 1400 and the inner diffused layer has a thickness of 20 to 100»m and a surface hardness (Hv) of 320 to 650.
- the nitrided hard layer comprising an alloy layer and a diffused layer, of the screw head portion and the like is removed from part of the surface of the screw.
- Methods of removal include a chemical method such as a dipping treatment in which the screw head and the like of the austenitic stainless steel screw are dipped in a mixed acid, for example, HCl + HNO3 or HF + HNO3, or in a single acid solution of HNO3 heated to about 60°C, and a mechanical method such as scouring.
- a chemical method such as a dipping treatment in which the screw head and the like of the austenitic stainless steel screw are dipped in a mixed acid, for example, HCl + HNO3 or HF + HNO3, or in a single acid solution of HNO3 heated to about 60°C, and a mechanical method such as scouring.
- the diameters of some portions of the austenitic stainless steel screw, such as the screw head and the neck part, from which the nitrided hard layer is removed, are relatively small.
- the diameters of the screw head and the neck part connected thereto are advantageously designed to be larger by the thickness of the nitrided hard layer. In this way, there is no deterioration in the breaking torque and thus no decrease in the tightening function of the screw.
- An austenitic stainless screw is held preliminarily in a fluorine- or fluoride-containing gas atmosphere to form a fluorinated layer on the steel surface, then heated in a nitriding atmosphere to remove the fluorinated layer and at the same time to convert the surface (the surface layer of the screw) to a nitrided layer.
- the nitrided layer over predetermined parts of the screw is removed to prevent rust on those parts.
- fluorine- or fluoride-containing gas used in the pretreatement prior to nitriding means a dilution of at least one fluorine source component selected from NF3, BF3, CF4, HF, SF6, F2, CH2F2, CH3F, C2F6, WF6, CHF3, SiF4 and the like in an inert gas such as N2.
- fluorine source components NF3 is most suitable for practical use since it is superior in reactivity, ease of handling and other aspects to the others.
- the screws are held in the above-mentioned fluorine- or fluoride-containing gas atmosphere at a temperature of, for example, 250 to 400°C in the case of NF3, for a preliminary treatment of the surface of an austenitic stainless screw and then subjected to nitriding (or carbonitriding) using a known nitriding gas such as ammonia.
- a known nitriding gas such as ammonia.
- F2 gas alone or a mixed gas composed of F2 gas and an inert gas is used as the fluorine- or fluoride-containing gas the above-mentioned holding temperature is arranged in the range of 100°C to 250°C.
- the concentration of the fluorine source component, such as NF3, in such fluorine- or fluoride-containing gas should amount to, for example, 1,000-100,000ppm, preferably 20,000-70,000ppm, more preferably 30,000-50,000ppm.
- the holding time in such a fluorine- or fluoride-containing gas atmosphere may appropriately be selected depending on the steel species, geometry and dimensions of the screws, the heating temperature and so forth, and is generally within the range of ten and odd minutes or scores of minutes.
- austenitic stainless screws X having a head portion A, a neck portion B and a thread portion C as shown in Fig. 1, for instance, are degreased and then charged into a heat treatment furnace 1 such as shown in Fig. 2.
- This furnace 1 is a pit furnace comprising an inner vessel 4 surrounded by a heater 3 disposed within an outer shell 2, with a gas inlet pipe 5 and an exhaust pipe 6 therein. Gas is supplied from cylinders 15 and 16 via flow meters 17, a valve 18 and the like into the gas inlet pipe 5. The inside atmosphere is stirred by means of a fan 8 driven by a motor 7.
- the screws X placed in a metallic container 11 are charged into the furnace.
- the reference numeral 13 indicates a vacuum pump and 14 a noxious substance eliminator.
- a fluorine- or fluoride-containing reaction gas for example, a mixed gas composed of NF3 and N2 is introduced into this furnace and heated, together with the works, at a predetermined reaction temperature.
- NF3 evolves fluorine in the nascent state, whereby the organic and inorganic contaminants on the surface of the screws are eliminated therefrom and at the same time this fluorine rapidly reacts with the base elements Fe and chromium on the surface and/or with oxides on the steel work surface, such as FeO, Fe3O4 and Cr2O3.
- a very thin fluorinated layer containing such compounds as FeF2, FeF3, CrF2, CrF4 and the like in the metal composition is formed on the surface, for example as follows: FeO + 2F ⁇ FeF2 + 1/2 O2 Cr2O3 + 4F ⁇ 2CrF2 + 3/2 O2
- fluorinated layer is stable at temperature up to 600°C and it is considered that the stable fluorinated layer prevents oxidized layer formation on the metal bases and absorption of O2 thereon until the subsequent step of nitriding.
- a fluorinated layer which is similarly stable, is formed on the furnace material surface as well and minimizes damage to the furnace material surface.
- the screws X thus treated with such fluorine- or fluoride-containing reaction gas are then heated at a nitriding temperature of 480°C-700°C.
- a nitriding temperature 480°C-700°C.
- NH3 or a mixed gas composed of NH3 and a carbon source gas e.g.
- an active metal base comprised of austenitic stainless steel, as shown, for example, by the following reaction equations: CrF4 + 2H3 ⁇ Cr + 4HF 2FeF3 + 3H2 ⁇ 2 Fe + 6HF
- active N atoms are adsorbed thereon, then enter the metal structure and diffuse therein and, as a result, a chemical compound layer (a nitrided hard layer) containing such nitrides as CrN, Fe2N, Fe3N and Fe4N is formed on the surface.
- the obtained nitrided hard layer comprises an alloy layer and a diffused layer and covers all the screw X shown in Fig. 1.
- This invention allows removal of the nitrided hard layer from, for example, the whole head portion A and a part of the neck portion B of the screw X shown in Fig. 1, while leaving the nitrided hard layer on the thread portion C and rest of the neck portion B as they are.
- the removal is, for example, conducted by heating HNO3-HF solution at about 50 °C, dipping the whole head portion A and a part of the neck portion B of the screw therein for about 10 to 120 minutes to melt and remove the nitrided hard layer.
- the nitrided layer of the whole head portion and a part of the neck portion is removed in this way to expose austenitic stainless steel.
- the screw X has sufficient corrosion resistance, resulting from that of austenitic stainless steel per se .
- the remaining nitrided hard layer of part of the neck portion B and the thread portion C has significantly improved hardness compared with that of austenitic stainless steel, giving the screw the same excellent tapping and tightening functions as carburized iron articles.
- nitriding is conducted by using NH3 or a mixed gas comprising NH3 and a gas containing a carbon source, but nitriding by glow discharge or by salt bath may be substituted for this type of nitriding.
- Cross recessed head tapping screws of SUS305, austenitic stainelss steel (4.2mm ⁇ x 19mm) were cleaned with trichloroethylene, then charged into a treatment furnace 1 as shown in Fig. 2, and held at 380°C for 15 minutes in an N2 gas atmosphere containing 5,000ppm of NF3 for fluoriding, then heated at 530°C, and nitriding treatment was carried out at that temperature for 3 hours while a mixed gas composed of 50% NH3 plus 50% N2 (hereinafter: % by volume) was introduced into the furnace.
- the works were then air-cooled and taken out of the furnace.
- the thus obtained screws had a nitrided hard layer with thickness of 40»m overall.
- the nitrided screw except for the head portion and a part of the neck portion to 4mm below the head was coated with vinyl choloride resin liquid and dried, to cover the screw with the coating.
- the screw was then dipped in 10% solution of HNO3 at 63°C for 15 minutes, taken out, washed with water and dried.
- the surface hardness (Hv) of the part of the tapping screw masked by the coating was 1000 to 1100.
- the head of the tapping screw from which the nitrided hard layer had been removed by the acid treatment had a surface hardness of 340 to 380.
- a salt spray test (Corrosion acceleration test) was conducted on the tapping screw and it was found that rust was not caused even after 2000 hours on the head and the part of the neck portion on which the austenitic stainless steel base was exposed. On the contrary, it was found that rust was caused after 6 hours on the part (mainly the thread) from which the nitrided hard layer was not removed.
- a drilling test was conducted on the above-mentioned screw and it was found that it had the same property as a conventional tapping screw (carburized iron steel works).
- Self drilling screws of SUS 305, austenitic stainless steel (hexagon head, 4.8mm ⁇ x 25mm) were nitrided as in Example 1.
- the nitrided hard layer was formed over the entire self-drilling screw; its thickness was 55»m.
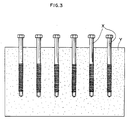
- the nitrided screw, except for the head and a part of the neck to 5mm below the head was dipped in vinyl chloride resin liquid and dried to cover the screw with a coating. Then a plurality of the screws were screwed into a polystyrene resin plate having a thickness of 30mm as shown in Fig. 3.
- a drilling test on the thus obtained screws was conducted against a steel plate with a thickness of 3.2mm (SPCC). Average drilling time in this case was 3.1 seconds. The time could be shortened by 20% on average compared with a conventional self-drilling screw (carburized iron works).
- the result of a salt spray test was the same as in Example 1.
- Self-drilling screws of austenitic stainless steel (hexagon head, 6.3mm ⁇ x 150mm) as shown in Fig. 1 were nitrided as in Example 1.
- the thus obtained self-drilling screw was covered with a nitrided hard layer overall; the thickness thereof was 75»m.
- Example 2 A salt spray test was conducted on the thus treated screw and the same result as in Example 1 was obtained, and the result of drilling test was the same as in Example 2.
- the breaking torque value of the thus obtained austenitic stainless self-drilling screw was examined. The value was lower by 7% than the austenitic stainless steel self-drilling screw the whole surface of which was covered by a nitrided hard layer, without the acid dipping treatment.
- austenitic stainless steel self drilling screws of which the diameters of the screw head and the neck portion were relatively large (about 150»m) were manufactured. They were nitrided and then dipped in acid to remove the nitrided hard layer from the screw head portion and neck portion. After eliminating the nitrided hard layer of the head and neck portions, the diameters of the head and neck portions were decreased.
- the breaking torque value of such screws was equal to an austenitic stainless steel self-drilling screw the whole surface of which was covered with a nitrided hard layer and the whole part having a diameter as previously designed respectively.
- a nitrided hard layer is removed from predetermined portions such as the head and neck portion, so that the austenitic stainless steel base is exposed on these portions.
- the head portion is exposed to the atmosphere in a tightened state and is affected by acid rain and the like, and the neck portion is in contact with acid rain and the like which has penetrated from outside.
- the portions from which the nitrided layer is removed maintain a good anti-corrosion property comparable with that of the austenitic stainless steel itself.
- the thread portion the hardness and the like are greatly improved by the nitrided hard layer, so that surface hardness and strength become approximately equal to those of carbon steel products, so that they are able to tap and tighten by themselves.
- the screw prior to nitriding the above-mentioned austenitic stainless steel screw, the screw is advantageously held in a fluorine- or fluoride-containing gas atmosphere to form a fluoride layer on the surface thereof. In that state the screw is nitrided, so that the formed nitrided layer is uniform and deep to give a hard austenitic stainless steel screw having good surface properties.
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Solid-Phase Diffusion Into Metallic Material Surfaces (AREA)
- Heat Treatment Of Articles (AREA)
- Forging (AREA)
- Extrusion Moulding Of Plastics Or The Like (AREA)
- Dental Tools And Instruments Or Auxiliary Dental Instruments (AREA)
Claims (4)
- Procédé de fabrication d'un article en acier inoxydable austénitique dur, comprenant les étapes consistant à : former une couche dure nitrurée à la surface d'un article en acier inoxydable austénitique, et éliminer la couche dure nitrurée dans des parties prédéterminées de l'article nitruré, pour mettre à nu l'acier inoxydable non nitruré.
- Procédé selon la revendication 1, dans lequel la couche dure nitrurée est formée en chauffant l'article en acier inoxydable austénitique dans une atmosphère nitrurante.
- Procédé selon la revendication 1 ou 2, dans lequel l'article en acier inoxydable austénitique est maintenu dans une atmosphère de gaz contenant du fluor ou un fluorure, pour former une couche de fluorure à sa surface, puis l'article fluoré est chauffé dans une atmosphère nitrurante pour former une couche dure nitrurée à la surface de l'article en acier inoxydable.
- Procédé selon l'une quelconque des revendications précédentes, dans lequel l'élimination de la couche dure nitrurée est réalisée en mettant la couche nitrurée en contact avec un acide fort.
Priority Applications (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE69115274T DE69115274T2 (de) | 1991-09-20 | 1991-09-20 | Eine harte, austenitische rostfreie Stahlschraube und Verfahren zu ihrer Herstellung. |
| DK91308660.9T DK0532806T3 (da) | 1991-09-20 | 1991-09-20 | Hård austenitisk rustfri stålskrue og en fremgangsmåde til fremstilling heraf |
| ES91308660T ES2082151T3 (es) | 1991-09-20 | 1991-09-20 | Tornillo de acero inoxidable austenitico duro y un metodo para fabricarlo. |
| AT91308660T ATE131217T1 (de) | 1991-09-20 | 1991-09-20 | Eine harte, austenitische rostfreie stahlschraube und verfahren zu ihrer herstellung. |
| EP91308660A EP0532806B1 (fr) | 1991-09-20 | 1991-09-20 | Une vis dure en acier austénitique inoxydable et procédé de sa fabrication |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP91308660A EP0532806B1 (fr) | 1991-09-20 | 1991-09-20 | Une vis dure en acier austénitique inoxydable et procédé de sa fabrication |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0532806A1 EP0532806A1 (fr) | 1993-03-24 |
| EP0532806B1 true EP0532806B1 (fr) | 1995-12-06 |
Family
ID=8208403
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP91308660A Expired - Lifetime EP0532806B1 (fr) | 1991-09-20 | 1991-09-20 | Une vis dure en acier austénitique inoxydable et procédé de sa fabrication |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP0532806B1 (fr) |
| AT (1) | ATE131217T1 (fr) |
| DE (1) | DE69115274T2 (fr) |
| DK (1) | DK0532806T3 (fr) |
| ES (1) | ES2082151T3 (fr) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2014122367A (ja) * | 2012-12-20 | 2014-07-03 | Daido Steel Co Ltd | 真空浸窒処理方法 |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2155078A5 (en) * | 1971-10-06 | 1973-05-18 | Kolomensky Teplovozostro | Spheroidal cast irons - strengthening by thermal and nitriding processes |
| AU3773478A (en) * | 1977-09-27 | 1980-01-10 | Deutsher Pty Ltd | Corrosion resistant self-drilling, thread-cutting screws |
| SE441933B (sv) * | 1984-02-14 | 1985-11-18 | Ibm Svenska Ab | Uppkolnings- och vermebehandlingsprocess for en maskindel, exempelvis en tryckhammare |
| EP0408168B1 (fr) * | 1989-07-10 | 1994-06-08 | Daidousanso Co., Ltd. | Procédé pour le prétraitement préalable de matériaux métalliques et procédé pour la nitruration d'acier |
-
1991
- 1991-09-20 DE DE69115274T patent/DE69115274T2/de not_active Expired - Lifetime
- 1991-09-20 EP EP91308660A patent/EP0532806B1/fr not_active Expired - Lifetime
- 1991-09-20 DK DK91308660.9T patent/DK0532806T3/da active
- 1991-09-20 AT AT91308660T patent/ATE131217T1/de not_active IP Right Cessation
- 1991-09-20 ES ES91308660T patent/ES2082151T3/es not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| ATE131217T1 (de) | 1995-12-15 |
| DK0532806T3 (da) | 1996-03-04 |
| DE69115274T2 (de) | 1996-05-30 |
| EP0532806A1 (fr) | 1993-03-24 |
| DE69115274D1 (de) | 1996-01-18 |
| ES2082151T3 (es) | 1996-03-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4975147A (en) | Method of pretreating metallic works | |
| EP0408168B1 (fr) | Procédé pour le prétraitement préalable de matériaux métalliques et procédé pour la nitruration d'acier | |
| US5013371A (en) | Method of nitriding steel | |
| US5340412A (en) | Method of fluorinated nitriding of austenitic stainless steel screw | |
| EP0588458B1 (fr) | Méthode pour la nitruration d'un acier à austénite inoxydable | |
| EP0479409B1 (fr) | Vis en acier inoxydable austénitique et méthode de sa fabrication | |
| US5254181A (en) | Method of nitriding steel utilizing fluoriding | |
| US5460875A (en) | Hard austenitic stainless steel screw and a method for manufacturing the same | |
| EP0516899B1 (fr) | Procédé de nitration d'acier | |
| US5419948A (en) | Hard austenitic stainless steel screw and a method for manufacturing the same | |
| US5650022A (en) | Method of nitriding steel | |
| EP0534010A1 (fr) | Traitement thermochimique de pièces de machines pour améliorer la résistance à la corrosion | |
| EP0532806A1 (fr) | Une vis dure en acier austénitique inoxydable et procédé de sa fabrication | |
| US5382318A (en) | Hard austenitic stainless steel screw and a method for manufacturing the same | |
| CN1041117C (zh) | 硬化的奥氏体不锈钢螺钉及其制造方法 | |
| JP2881111B2 (ja) | 鋼の窒化方法 | |
| KR100213404B1 (ko) | 경질 오스테나이트계 스테인레스 나사 및 그 제조방법 | |
| JP2686001B2 (ja) | オーステナイト系ステンレス製硬質ねじ | |
| JP2918765B2 (ja) | 表面が窒化硬化されたニッケル合金製品 | |
| CA2043872C (fr) | Procede de nitruration de l'acier | |
| JP3005953B2 (ja) | 鋼の窒化方法 | |
| JP3428776B2 (ja) | 鋼の窒化方法 | |
| KR980009701A (ko) | 건축용 석재 고정재 | |
| WO1997003227A1 (fr) | Traitement de surface d'objets en aluminium et en alliages d'aluminium | |
| KR19990015775U (ko) | 플라즈마를 이용한 이온 침탄로 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT CH DE DK ES FR GB IT LI NL SE |
|
| 17P | Request for examination filed |
Effective date: 19930817 |
|
| R17P | Request for examination filed (corrected) |
Effective date: 19930817 |
|
| 17Q | First examination report despatched |
Effective date: 19940310 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: DAIDO HOXAN INC. |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT CH DE DK ES FR GB IT LI NL SE |
|
| REF | Corresponds to: |
Ref document number: 131217 Country of ref document: AT Date of ref document: 19951215 Kind code of ref document: T |
|
| ITF | It: translation for a ep patent filed | ||
| REF | Corresponds to: |
Ref document number: 69115274 Country of ref document: DE Date of ref document: 19960118 |
|
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: BOVARD AG PATENTANWAELTE |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2082151 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 19980914 Year of fee payment: 8 Ref country code: DK Payment date: 19980914 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 19980921 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990920 Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990920 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990921 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PFA Free format text: DAIDO HOXAN INC. TRANSFER- AIR WATER INC. |
|
| NLT1 | Nl: modifications of names registered in virtue of documents presented to the patent office pursuant to art. 16 a, paragraph 1 |
Owner name: AIR WATER INC. |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20001013 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050920 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20070913 Year of fee payment: 17 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20070916 Year of fee payment: 17 Ref country code: SE Payment date: 20070905 Year of fee payment: 17 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20090401 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 20090401 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080930 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080930 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20090916 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20090917 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20091012 Year of fee payment: 19 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080921 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20100920 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20110531 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 69115274 Country of ref document: DE Effective date: 20110401 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110401 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100920 |