EP0591732A1 - Procédé pour la fabrication d'une clé ouverte - Google Patents
Procédé pour la fabrication d'une clé ouverte Download PDFInfo
- Publication number
- EP0591732A1 EP0591732A1 EP93114959A EP93114959A EP0591732A1 EP 0591732 A1 EP0591732 A1 EP 0591732A1 EP 93114959 A EP93114959 A EP 93114959A EP 93114959 A EP93114959 A EP 93114959A EP 0591732 A1 EP0591732 A1 EP 0591732A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- key
- spanner
- polygonal
- mouth
- nut
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B25—HAND TOOLS; PORTABLE POWER-DRIVEN TOOLS; MANIPULATORS
- B25B—TOOLS OR BENCH DEVICES NOT OTHERWISE PROVIDED FOR, FOR FASTENING, CONNECTING, DISENGAGING, OR HOLDING
- B25B13/00—Spanners; Wrenches
- B25B13/02—Spanners; Wrenches with rigid jaws
- B25B13/04—Spanners; Wrenches with rigid jaws of ring jaw type
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21K—MAKING FORGED OR PRESSED METAL PRODUCTS, e.g. HORSE-SHOES, RIVETS, BOLTS OR WHEELS
- B21K5/00—Making tools or tool parts, e.g. pliers
- B21K5/16—Making tools or tool parts, e.g. pliers tools for turning nuts
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B25—HAND TOOLS; PORTABLE POWER-DRIVEN TOOLS; MANIPULATORS
- B25B—TOOLS OR BENCH DEVICES NOT OTHERWISE PROVIDED FOR, FOR FASTENING, CONNECTING, DISENGAGING, OR HOLDING
- B25B13/00—Spanners; Wrenches
- B25B13/02—Spanners; Wrenches with rigid jaws
- B25B13/08—Spanners; Wrenches with rigid jaws of open jaw type
Definitions
- the present invention relates to a method for producing an open ring key, and the invention further relates to an open ring key which is produced using the proposed method.
- Keys with an open ring are tools that are mainly used in the assembly of hydraulic systems, for example in the braking systems of a motor vehicle. These tools, which are usually designed as polygonal keys, have a mouth-like opening on their front and in accordance with the surfaces that delimit the polygonal key mouth, an open contact surface is provided, which is directed towards the center of the key mouth. This makes it possible when using such a key to push the tool over the open mouth onto the hydraulic line, which is designed, for example, as a tube, and then to move the key along the hydraulic pipe.
- the polygonal recess of the key with an open ring comes into operative connection with the nut for fixing the pipeline and, thanks to the support surface provided on the circumference, which is arranged on one side of the ring key provided with the opening, the key's mouth is unintentionally loosened or slipping off the mother because the thickened circumferential surface of the key rests on the mother. This prevents an unwanted loosening of the key mouth from the mother.
- the desired polygonal key shape is produced on the key head as a non-continuous, cup-shaped, flat body.
- each blank of the key head is to be subjected to machining, with which the bottom of the cup-shaped raw body is cut off, in order to create a contact surface for the polygonal structure of the key head on the nut.
- the object of the above invention is to address the disadvantages to avoid the prior art and to propose a new method for the production of open ring keys, with which method it is possible to produce an open ring key economically, the polygonal mouth of which has the greatest precision on the inside.
- the advantage is achieved that the raw body of the open ring key can be produced quickly and economically by a hot pressing process or a forging process, in accordance with the production methods for known keys.
- the exact dimensions, as well as the inner circumferential shape of the key mouth, as in a conventional fork wrench, are processed in one work process, but additionally by a subsequent plastic deformation, e.g. B. by a pressing or stamping process, which can be carried out with a simple auxiliary tool, it is possible to produce the entire circumferential thickening that protrudes to the inside of the key mouth. This ensures a secure support of the open mouth of the ring wrench, e.g. B. on a hex nut.
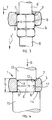
- the open ring key designed according to the invention is identified overall by 1 and has an extension 2 or a stem, at the end of which a fork-like head 3 is provided which circumscribes the mouth 4 of the open ring key.
- the key 1 has an opening 5 on its front to the passage, z. B. a hydraulic line 8 ', which is shown with chain lines.
- the key head 3 On its inside, the key head 3 has side walls 6, which circumscribe a hexagon, an octagon or any polygon or another suitable profile, which has a clear width (a) corresponding to the dimensions of the nut with which the key 1 is positively connected to be brought.
- a thickening 7 which extends in the circumferential direction, the thickening 7 projecting towards the inside of the key head 3.
- the thickening forms a support for the key head 3 as soon as it is placed on a nut 9 to be actuated (FIG. 3).
- Fig. 3 shows a hydraulic line 8, with the aid of a nut 9, which is usually made of aluminum or a other relatively light and soft material.
- the key 1, 3 was used as a blank, e.g. B. manufactured by a hot pressing process or a forging process, an excess metal was left in accordance with the walls 6 (inside width a).
- the inner key mouth 4 of the head 3 is subjected to precision machining, e.g. B. subjected to a clearing process. This machining removes the remaining excess material and determines the dimension of the clear width (a) with very high precision.
- the thickening 7 necessary in the circumferential direction of the key mouth for securely resting the key head 3 on a nut is produced.
- the head 3 of the key 1 is placed in a pressing tool 10, the raised part 11 of which fills the free space 4 of the head 3 of the key 1, which rests on a seat 14.
- the raised part 11 has a height that is smaller than the thickness (b) of the key head 3.
- the raised part 11 has a bevel 12 which extends in the circumferential direction.
- the tool 10, 12 is assigned a press ram 13 which is wider than the clear width (a) of the key head.
- the material forming the head 3 of the key 1 is plastically deformed.
- the plastically deformed material is displaced into the annular peripheral chamber formed by the chamfer 12, which is formed between the side walls 6 of the key and the chamfer 12 provided on the circumferential side.
- an economical method e.g. B. a pressing process or a forging process for the production of the raw key body is used. Initially, there is no need to create the supporting surface or thickening.
- the key blanks produced in this way are then subjected to suitable precision machining, e.g. B. subjected to a broaching process, thus creating a jaw opening (a) with high precision.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Forging (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| ITMI922184A IT1255825B (it) | 1992-09-24 | 1992-09-24 | Procedimento per la realizzazione di una chiave ad anello aperto |
| ITMI922184 | 1992-09-24 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0591732A1 true EP0591732A1 (fr) | 1994-04-13 |
| EP0591732B1 EP0591732B1 (fr) | 1998-07-08 |
Family
ID=11363989
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP93114959A Expired - Lifetime EP0591732B1 (fr) | 1992-09-24 | 1993-09-16 | Procédé pour la fabrication d'une clé ouverte |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0591732B1 (fr) |
| DE (1) | DE59308739D1 (fr) |
| ES (1) | ES2117686T3 (fr) |
| IT (1) | IT1255825B (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2362594A (en) * | 2000-05-22 | 2001-11-28 | Hand Tool Design Corp | Box spanner |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104282505A (zh) * | 2013-07-12 | 2015-01-14 | 上海工程技术大学 | 用于一体化螺钉螺母调节锁紧装置的外套筒结构 |
Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2715347A (en) * | 1952-12-02 | 1955-08-16 | Tubing Appliance Company Inc | Webbed open-end box wrench |
| US2774259A (en) * | 1955-07-11 | 1956-12-18 | Frank T Caulkins | Method of making box wrenches |
| US3121356A (en) * | 1962-06-14 | 1964-02-18 | Henderson G Davis | Slip-proof wrench |
| FR2227093A1 (en) * | 1973-04-27 | 1974-11-22 | Wilmonda Manuf Outillage | Double open headed spanner for pipe couplings - series of flats on one head is rotated 30 degrees w.r.t. those on second head |
| CA1257487A (fr) * | 1986-05-13 | 1989-07-18 | Edward Izatt | Cle fermee |
-
1992
- 1992-09-24 IT ITMI922184A patent/IT1255825B/it active IP Right Grant
-
1993
- 1993-09-16 EP EP93114959A patent/EP0591732B1/fr not_active Expired - Lifetime
- 1993-09-16 ES ES93114959T patent/ES2117686T3/es not_active Expired - Lifetime
- 1993-09-16 DE DE59308739T patent/DE59308739D1/de not_active Expired - Fee Related
Patent Citations (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2715347A (en) * | 1952-12-02 | 1955-08-16 | Tubing Appliance Company Inc | Webbed open-end box wrench |
| US2774259A (en) * | 1955-07-11 | 1956-12-18 | Frank T Caulkins | Method of making box wrenches |
| US3121356A (en) * | 1962-06-14 | 1964-02-18 | Henderson G Davis | Slip-proof wrench |
| FR2227093A1 (en) * | 1973-04-27 | 1974-11-22 | Wilmonda Manuf Outillage | Double open headed spanner for pipe couplings - series of flats on one head is rotated 30 degrees w.r.t. those on second head |
| CA1257487A (fr) * | 1986-05-13 | 1989-07-18 | Edward Izatt | Cle fermee |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2362594A (en) * | 2000-05-22 | 2001-11-28 | Hand Tool Design Corp | Box spanner |
Also Published As
| Publication number | Publication date |
|---|---|
| DE59308739D1 (de) | 1998-08-13 |
| ES2117686T3 (es) | 1998-08-16 |
| IT1255825B (it) | 1995-11-17 |
| ITMI922184A0 (it) | 1992-09-24 |
| ITMI922184A1 (it) | 1994-03-24 |
| EP0591732B1 (fr) | 1998-07-08 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0521354B1 (fr) | Arbre à cames pour le contrôle des soupapes dans les moteurs à combustion interne | |
| DE2225466C3 (de) | Vorrichtung zur Herstellung eines aus Blech bestehenden Ketten- oder Zahnrades | |
| DE3223004A1 (de) | Lenkspindel fuer lenkvorrichtungen fuer kraftfahrzeuge sowie verfahren zur herstellung einer solchen lenkspindel | |
| DE69106760T2 (de) | Verfahren zum Herstellen eines Reibringes. | |
| EP0759134A1 (fr) | Systeme de fermeture pour obturer des conduites d'acheminement de substances sous pression dans un boitier | |
| EP1108483B1 (fr) | Procédé et dispositif pour le fluotournage | |
| EP2479442A1 (fr) | Elément de fonction sous la forme d'un élément de compression | |
| DE19520099C2 (de) | Rohrverbindung und Verfahren zu ihrer Herstellung | |
| EP1252947B1 (fr) | Procédé de fabrication d'un élément d'essieu pour un véhicule automobile | |
| EP2224143A1 (fr) | Ecrou, raccordement de vis, connexion de profilé, ainsi que procédé de fabrication d'un écrou | |
| DE102010011711B4 (de) | Verfahren und Vorrichtung zur spanlosen Herstellung von Verbindungs-, Befestigungs- oder Verschlusselementen aus Metall mit Außengewinde | |
| EP0591732B1 (fr) | Procédé pour la fabrication d'une clé ouverte | |
| DE202009017864U1 (de) | Stanz-Prägeniet | |
| DE19650453B4 (de) | Verfahren zur Herstellung einer Zusammenbau-Mutter sowie nach dem Verfahren hergestellte Zusammenbau-Mutter | |
| DE4004008C1 (fr) | ||
| DE19855753A1 (de) | Verfahren und Vorrichtung zum hydraulischen Umformen von Werkstücken | |
| DE2638560C3 (de) | Sicherungsmutter | |
| EP1070896B1 (fr) | Procédé de fabrication d'un élément d emmanchement par pressage | |
| DE19941577A1 (de) | Rohrverbindung und Verfahren zu ihrer Herstellung | |
| EP0579005B1 (fr) | Procédé, dispositif et matrice pour la fabrication d'une pièce ayant une section profilée | |
| DE577930C (de) | Herstellung von einseitig oder beiderseitig abgefasten Schraubenmuttern, Bolzenkoepfen o. dgl. | |
| DE468110C (de) | Herstellung von Aufdornstehbolzen | |
| DE10138442C1 (de) | Verfahren zur Herstellung eines metallischen Pressfittingelementes | |
| EP0990769A1 (fr) | Procédé de fabrication d'un cylindre comportant une extension longitudinale | |
| EP3863780A1 (fr) | Procédé et dispositifs pour matricer des structures superficielles dans une face intérieure d'un tube ou d'une tige de soupape d'une soupape-champignon et soupape champignon à structure intérieure matricée |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE ES FR GB IT NL |
|
| 17P | Request for examination filed |
Effective date: 19940527 |
|
| 17Q | First examination report despatched |
Effective date: 19951019 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES FR GB IT NL |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19980720 |
|
| REF | Corresponds to: |
Ref document number: 59308739 Country of ref document: DE Date of ref document: 19980813 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2117686 Country of ref document: ES Kind code of ref document: T3 |
|
| ITF | It: translation for a ep patent filed | ||
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19990928 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 19990930 Year of fee payment: 7 Ref country code: ES Payment date: 19990930 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19991004 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19991015 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20000916 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20000917 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20010401 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20000916 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20010531 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 20010401 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20010601 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20011011 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050916 |