EP0670190B1 - Moule de fonderie et son procédé de réalisation - Google Patents
Moule de fonderie et son procédé de réalisation Download PDFInfo
- Publication number
- EP0670190B1 EP0670190B1 EP95400426A EP95400426A EP0670190B1 EP 0670190 B1 EP0670190 B1 EP 0670190B1 EP 95400426 A EP95400426 A EP 95400426A EP 95400426 A EP95400426 A EP 95400426A EP 0670190 B1 EP0670190 B1 EP 0670190B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- substrate
- mold
- coating
- keying
- layer
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims description 15
- 230000008569 process Effects 0.000 title description 4
- 239000000758 substrate Substances 0.000 claims description 31
- 238000000576 coating method Methods 0.000 claims description 29
- 239000011248 coating agent Substances 0.000 claims description 24
- 239000010410 layer Substances 0.000 claims description 16
- 238000004519 manufacturing process Methods 0.000 claims description 12
- 229910045601 alloy Inorganic materials 0.000 claims description 9
- 239000000956 alloy Substances 0.000 claims description 9
- 239000000203 mixture Substances 0.000 claims description 9
- 238000000151 deposition Methods 0.000 claims description 8
- 239000000463 material Substances 0.000 claims description 8
- 229910052751 metal Inorganic materials 0.000 claims description 8
- 239000002184 metal Substances 0.000 claims description 8
- 229910000838 Al alloy Inorganic materials 0.000 claims description 7
- 229910052782 aluminium Inorganic materials 0.000 claims description 6
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims description 6
- 229910052593 corundum Inorganic materials 0.000 claims description 6
- 229910052596 spinel Inorganic materials 0.000 claims description 6
- 239000011029 spinel Substances 0.000 claims description 6
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 claims description 5
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 claims description 5
- 239000011651 chromium Substances 0.000 claims description 5
- 239000010431 corundum Substances 0.000 claims description 5
- 230000008021 deposition Effects 0.000 claims description 5
- KZHJGOXRZJKJNY-UHFFFAOYSA-N dioxosilane;oxo(oxoalumanyloxy)alumane Chemical compound O=[Si]=O.O=[Si]=O.O=[Al]O[Al]=O.O=[Al]O[Al]=O.O=[Al]O[Al]=O KZHJGOXRZJKJNY-UHFFFAOYSA-N 0.000 claims description 5
- 229910052863 mullite Inorganic materials 0.000 claims description 5
- 239000011241 protective layer Substances 0.000 claims description 5
- 229910052727 yttrium Inorganic materials 0.000 claims description 5
- 229910052804 chromium Inorganic materials 0.000 claims description 4
- VWQVUPCCIRVNHF-UHFFFAOYSA-N yttrium atom Chemical compound [Y] VWQVUPCCIRVNHF-UHFFFAOYSA-N 0.000 claims description 4
- 229910000990 Ni alloy Inorganic materials 0.000 claims description 3
- 229910052759 nickel Inorganic materials 0.000 claims description 3
- SIWVEOZUMHYXCS-UHFFFAOYSA-N oxo(oxoyttriooxy)yttrium Chemical compound O=[Y]O[Y]=O SIWVEOZUMHYXCS-UHFFFAOYSA-N 0.000 claims description 3
- 239000000126 substance Substances 0.000 claims description 3
- 238000005422 blasting Methods 0.000 claims description 2
- QFXZANXYUCUTQH-UHFFFAOYSA-N ethynol Chemical group OC#C QFXZANXYUCUTQH-UHFFFAOYSA-N 0.000 claims description 2
- 239000002245 particle Substances 0.000 claims description 2
- 239000011819 refractory material Substances 0.000 claims description 2
- 229910003112 MgO-Al2O3 Inorganic materials 0.000 claims 1
- 238000010438 heat treatment Methods 0.000 claims 1
- 235000019592 roughness Nutrition 0.000 claims 1
- 229910000831 Steel Inorganic materials 0.000 description 7
- 238000002360 preparation method Methods 0.000 description 7
- 239000010959 steel Substances 0.000 description 7
- 238000005266 casting Methods 0.000 description 4
- 229910018072 Al 2 O 3 Inorganic materials 0.000 description 3
- 239000007788 liquid Substances 0.000 description 3
- CPLXHLVBOLITMK-UHFFFAOYSA-N magnesium oxide Inorganic materials [Mg]=O CPLXHLVBOLITMK-UHFFFAOYSA-N 0.000 description 3
- 239000000395 magnesium oxide Substances 0.000 description 3
- 238000000465 moulding Methods 0.000 description 3
- 230000009467 reduction Effects 0.000 description 3
- PNEYBMLMFCGWSK-UHFFFAOYSA-N aluminium oxide Inorganic materials [O-2].[O-2].[O-2].[Al+3].[Al+3] PNEYBMLMFCGWSK-UHFFFAOYSA-N 0.000 description 2
- 230000015556 catabolic process Effects 0.000 description 2
- 239000000919 ceramic Substances 0.000 description 2
- 238000006731 degradation reaction Methods 0.000 description 2
- 238000000605 extraction Methods 0.000 description 2
- 230000003993 interaction Effects 0.000 description 2
- 238000010112 shell-mould casting Methods 0.000 description 2
- 229910001018 Cast iron Inorganic materials 0.000 description 1
- 229910000531 Co alloy Inorganic materials 0.000 description 1
- 229910000599 Cr alloy Inorganic materials 0.000 description 1
- 229910000676 Si alloy Inorganic materials 0.000 description 1
- 229910000946 Y alloy Inorganic materials 0.000 description 1
- CSDREXVUYHZDNP-UHFFFAOYSA-N alumanylidynesilicon Chemical compound [Al].[Si] CSDREXVUYHZDNP-UHFFFAOYSA-N 0.000 description 1
- 239000004411 aluminium Substances 0.000 description 1
- RFEISCHXNDRNLV-UHFFFAOYSA-N aluminum yttrium Chemical compound [Al].[Y] RFEISCHXNDRNLV-UHFFFAOYSA-N 0.000 description 1
- 230000004888 barrier function Effects 0.000 description 1
- 239000011324 bead Substances 0.000 description 1
- 239000010941 cobalt Substances 0.000 description 1
- GUTLYIVDDKVIGB-UHFFFAOYSA-N cobalt atom Chemical compound [Co] GUTLYIVDDKVIGB-UHFFFAOYSA-N 0.000 description 1
- 239000000470 constituent Substances 0.000 description 1
- 230000006378 damage Effects 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- UAMZXLIURMNTHD-UHFFFAOYSA-N dialuminum;magnesium;oxygen(2-) Chemical compound [O-2].[O-2].[O-2].[O-2].[Mg+2].[Al+3].[Al+3] UAMZXLIURMNTHD-UHFFFAOYSA-N 0.000 description 1
- 230000008030 elimination Effects 0.000 description 1
- 238000003379 elimination reaction Methods 0.000 description 1
- 230000005484 gravity Effects 0.000 description 1
- 238000005461 lubrication Methods 0.000 description 1
- 239000000843 powder Substances 0.000 description 1
- 230000002028 premature Effects 0.000 description 1
- 230000001737 promoting effect Effects 0.000 description 1
- 230000001681 protective effect Effects 0.000 description 1
- 230000033764 rhythmic process Effects 0.000 description 1
- 230000035939 shock Effects 0.000 description 1
- 238000007711 solidification Methods 0.000 description 1
- 230000008023 solidification Effects 0.000 description 1
- 239000002904 solvent Substances 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
- 230000001629 suppression Effects 0.000 description 1
- 239000000725 suspension Substances 0.000 description 1
- 238000007751 thermal spraying Methods 0.000 description 1
- 229910052721 tungsten Inorganic materials 0.000 description 1
- 229910001845 yogo sapphire Inorganic materials 0.000 description 1
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
- C23C4/02—Pretreatment of the material to be coated, e.g. for coating on selected surface areas
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C3/00—Selection of compositions for coating the surfaces of moulds, cores, or patterns
Definitions
- the present invention relates to a mold for foundry for aluminum alloys, as well as a process for its realization.
- This refractory layer has several functions.
- this refractory lining protects the shell and thus prevents its premature destruction.
- this coating constitutes a interface between the mold and the liquid alloy, which minimizes interactions.
- such a coating ensures certain thermal exchanges and participates in the control of the directed solidification.
- the document EP A 0 212 157 describes a foundry mold for the production of grids of lead, comprising a metal substrate coated with a protective layer, said layer having a ceramic refractory lining, as well as a bonding underlayment to base of a chromium, cobalt or nickel alloy, interposed between the coating ceramic refractory and metal substrate.
- a mold of Foundry for aluminum alloys is subject to strong thermal differences. Before the casting operation it is heated by burners of so as to be kept at a temperature of the order of 350 ° C. Then, the alloy is poured into it at a temperature which is around 680 ° C in the case of alloys aluminum. Mold wall temperatures therefore vary between 350 ° C and 680 ° C each time a part is cast, the rates of casting being able to hit the rhythm of one pour every five minutes. These thermal differences between the substrate and its coating induce differences in expansion which, by their repetition, destroy said coating.
- the invention provides a foundry mold for aluminum alloys comprising a metal substrate coated with a protective layer, said layer having a coating of a refractory material inert with respect to the cast metal, as well a bonding sub-layer interposed between the coating and the substrate, characterized in that the coating is made of a material chosen from the group comprising mullite, yttrium oxide and MgO-Al 2 O 3 mixtures , such as spinel, and in that the bonding layer is made of an alloy of nickel, chromium, aluminum and yttrium.
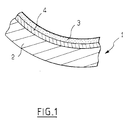
- the mold 1 shown in this figure includes a substrate 2, as well as a coating 3. Between the substrate 2 and the coating 3 is interposed a layer intermediate 4.
- the substrate 2 is for example made of steel Z38CDV05, this steel being conventionally used for making foundry molds with good resistance to thermal shock.
- the material of the refractory lining 3 is chosen for its insulating, refractory and inert qualities vis-à-vis cast alloys. It thus resists chemical aggressiveness of cast alloys and allows avoid tinning.
- the intermediate layer 4 constitutes, for the refractory lining 3, a bonding sub-layer. It is made of a material which is chosen so that said refractory lining 3 does not deteriorate during molding cycles, by difference in expansion thermal with substrate 2.
- This bonding underlayer 4 is made of an alloy by Ni Cr Al Y (Nickel Chrome Aluminum Yttrium), by example with the following weight percentages: 67% Ni, 22% Cr, 10% W Al, 1% Y and has a coefficient of thermal expansion close to that of substrate 2 and allowing good attachment of the coating 3 refractory.
- the thermal coefficients of expansion of the steel of the substrate 2 and of the various constituents mentioned above for the sub-layer 4 and the coating 3, are the following: (in m / mK) Z38CDV5 between 12.6 and 13.2.10 -6 Mullite 5.10 -6 Al 2 O 3 8.10 -6 MgO 12 to 16.10 -6 Spinel 8.3.10 -6 Y 2 O 3 8.10 -6 Ni Cr Al Y 15.2.10 -6 (in the above composition)
- the thickness of the underlay 4 of Ni Cr Al Y alloy can be included between 0.02 and 0.2 mm, that of the coating 3 between 0.01 and 0.11 mm when in alumina-magnesia and in particular between 0.01 and 0.03 mm when it is spinel.
- Cohesion, roughness, hardness of the layer protective thus produced by the coating 3 and the undercoat 4 are such that we do not observe degradation of the mold surface compared to that observed on a poteyé mold in a traditional way. The best results are obtained with coatings 3 of spinel.
- the corundumization operation is carried out by means of a numerically controlled machine.
- Surface condition obtained for the parts to be coated, in particular their roughness, is very precisely controlled by playing on the distance between the corundumization nozzle and the part to to cover, as well as the angle of incidence according to which the corundum particles are projected onto the part.
- This preparation is preferably carried out just before the deposition of the sublayer 4 hooking and refractory lining 3, so as not to not give the coated part time to oxidize or get polluted.
- the operations of deposition are carried out by thermal spraying by torch plasma.
- the plasma torch is manipulated by a robot and controlled by a programmable controller, which allows repeatability of operations.
- the deposit can also be carried out using an oxy-acetylene torch.
- the material to deposit is placed on the substrate 2 in the form of a bead or powder, said substrate 2 being brought to high temperature (around or above 600 ° C), so as to promote the chemical bonds between the underlay attachment 4 and the substrate 2.
- the deposits of the undercoat 4 for hanging and covering 3 can be produced by the plasma torch on a substrate 2 brought to high temperature (around or above 600 ° C).
- the invention has been described for the foundry of aluminum alloys in gravity shell. She of course applies generally to any molding in shell, and in particular in shell molding under high pressure or under low pressure.
- An advantageous application of the invention is the manufacture of parts for motor vehicles.
Landscapes
- Engineering & Computer Science (AREA)
- Chemical & Material Sciences (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Plasma & Fusion (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Other Surface Treatments For Metallic Materials (AREA)
- Coating By Spraying Or Casting (AREA)
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
Description
- l'oxyde d'yttrium Y2O3,
- la mullite, de composition 3Al2O3 - 2SiO2 ,
- les mélanges MgO - Al2O3, et parmi ceux-ci plus particulièrement la spinelle de composition Mg Al2O4.
| Z38CDV5 | entre 12,6 et 13,2.10-6 |
| Mullite | 5.10-6 |
| Al2O3 | 8.10-6 |
| MgO | 12 à 16.10-6 |
| Spinelle | 8,3.10-6 |
| Y2O3 | 8.10-6 |
| Ni Cr Al Y | 15,2.10-6 (dans la composition ci-dessus) |
- des gains substantiels au niveau du coût de fabrication des pièces produites en aluminium coulées en coquille ;
- une dotation moins importante en nombre de moules pour assurer la production d'une pièce donnée du fait de la suppression du poteyage (aujourd'hui : 8 moules en fabrication, pour 2 moules en poteyage), ce qui se traduit par une réduction des investissements pour fabriquer les pièces de fonderie ;
- une diminution de la masse des pièces produites du fait de la réduction possible des dépouilles nécessaires à l'extraction de la pièce du moule, les moules poteyés nécessitant quant à eux des dépouilles importantes de façon à éviter la dégradation rapide du poteyage à chaque démoulage de pièce ;
- l'utilisation de matériaux moins chers que ceux utilisés actuellement pour réaliser des parties de moules du fait de la résistance des dépôts.
Claims (11)
- Moule de fonderie pour alliages d'aluminium comportant un substrat métallique (2) revêtu d'une couche protectrice (3,4), ladite couche présentant un revêtement (3) en un matériau réfractaire inerte vis-à-vis du métal coulé, ainsi qu'une sous-couche (4) d'accrochage interposée entre le revêtement (3) et le substrat (2), ledit revêtement (3) étant en un matériau choisi dans le groupe comprenant la mullite, l'oxyde d'yttrium et les mélanges MgO-Al2O3, tels que la spinelle, caractérisé en ce que la couche d'accrochage est en un alliage de nickel, de chrome, d'aluminium et d'yttrium.
- Moule de fonderie selon la revendication 1, caractérisé en ce que ledit alliage présente la composition pondérale suivante : 67 % de nickel, 22 % de chrome, 10 % d'aluminium et 1 % d'yttrium.
- Procédé de réalisation d'un moule (1) selon l'une quelconque des revendications 1 et 2, caractérisé en ce qu'il comprend les étapes suivantes :a) préparation de la surface du substrat (2) métallique ;b) dépôt de la sous-couche (4) d'accrochage ; etc) dépôt du revêtement (3).
- Procédé selon la revendication 3, caractérisé en ce que l'étape a) consiste à éliminer de la surface du substrat (2) une éventuelle couche d'oxyde et à créer des rugosités facilitant le dépôt de la sous-couche (4) d'accrochage.
- Procédé selon la revendication 4, caractérisé en ce que l'étape a) comprend une opération de grenaillage de la surface du substrat (2) avec des particules de corindon.
- Procédé selon l'une des revendications 3 à 5, caractérisé en ce que les étapes b) et c) sont effectuées suffisamment rapidement après l'étape a) pour que le substrat (2) n'ait pas le temps de s'oxyder.
- Procédé selon l'une des revendications 3 à 6, caractérisé en ce que l'étapes b) et/ou l'étape c) sont effectuées à l'aide d'un appareil à torche à plasma.
- Procédé selon la revendication 7, caractérisé en ce que la torche est montée sur un robot et pilotée par un automate programmable afin d'obtenir des dépôts répétitifs.
- Procédé selon l'une des revendications 3 à 8, caractérisé en ce qu'il comprend une étape supplémentaire d), effectuée après l'étape a) et avant l'étape b), consistant à chauffer le substrat (2) à une température suffisante pour favoriser une liaison chimique entre le substrat (2) et la sous-couche (4) d'accrochage.
- Procédé selon la revendication 9, caractérisé en ce que ladite température est supérieure ou égale à 600°C.
- Procédé selon l'une des revendications 3 à 10, caractérisé en ce que l'étape b) et/ou l'étape c) sont effectuées à l'aide d'un appareil tel qu'un chalumeau oxyacétylénique.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9402327A FR2716898B1 (fr) | 1994-03-01 | 1994-03-01 | Pièce, telle qu'un moule de fonderie, et son procédé de réalisation. |
| FR9402327 | 1994-03-01 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0670190A1 EP0670190A1 (fr) | 1995-09-06 |
| EP0670190B1 true EP0670190B1 (fr) | 2000-05-03 |
Family
ID=9460539
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP95400426A Expired - Lifetime EP0670190B1 (fr) | 1994-03-01 | 1995-02-28 | Moule de fonderie et son procédé de réalisation |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0670190B1 (fr) |
| DE (1) | DE69516566T2 (fr) |
| ES (1) | ES2146294T3 (fr) |
| FR (1) | FR2716898B1 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101456061B (zh) * | 2007-12-10 | 2010-08-11 | 洛阳双瑞精铸钛业有限公司 | 一种提高石墨型钛合金铸件质量的辅助工艺 |
Families Citing this family (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2736850B1 (fr) * | 1995-07-19 | 1997-10-10 | Peugeot | Moule de fonderie et procede de realisation d'un tel moule |
| FR2850891B1 (fr) * | 2003-02-06 | 2006-08-04 | Acierie Et Fonderie De La Haut | Mode de protection des outils en contact avec les metaux et verres en fusion |
| ITMO20050131A1 (it) * | 2005-05-27 | 2006-11-28 | T W R Sas Di Mario Doda E C | Stampo per la formatura di manufatti ceramici. |
| DE102009009559B4 (de) | 2009-02-19 | 2022-02-17 | Ceranovis Gmbh | Verfahren zum Verlängern der Standzeit von technischen Oberflächen |
| CN110408880A (zh) * | 2019-09-02 | 2019-11-05 | 中国科学院金属研究所 | 一种大气等离子喷涂技术制备y+y2o3/y2o3复合涂层的方法 |
| CN117512492B (zh) * | 2024-01-04 | 2024-04-16 | 北矿新材科技有限公司 | 微孔弥散型高温可磨耗封严涂层及其制备方法 |
Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0212157A2 (fr) * | 1985-08-20 | 1987-03-04 | VARTA Batterie Aktiengesellschaft | Dispositif de coulée de grillages de plomb pour plaques d'accumulateurs et procédé pour sa fabrication |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS63153256A (ja) * | 1986-12-17 | 1988-06-25 | Honda Motor Co Ltd | 銅金型表面のコ−テイング方法 |
| US4900640A (en) * | 1988-04-19 | 1990-02-13 | Inco Limited | Low coefficient of expansion alloys having a thermal barrier |
| JP2695835B2 (ja) * | 1988-05-06 | 1998-01-14 | 株式会社日立製作所 | セラミック被覆耐熱部材 |
| US5034284A (en) * | 1990-05-10 | 1991-07-23 | United Technologies Corporation | Thermal fatigue resistant coatings |
| JP3066812B2 (ja) * | 1991-10-09 | 2000-07-17 | 黒崎播磨株式会社 | 2層以上のコーティングを有する低融点金属の鋳造用器具 |
-
1994
- 1994-03-01 FR FR9402327A patent/FR2716898B1/fr not_active Expired - Fee Related
-
1995
- 1995-02-28 EP EP95400426A patent/EP0670190B1/fr not_active Expired - Lifetime
- 1995-02-28 DE DE1995616566 patent/DE69516566T2/de not_active Expired - Fee Related
- 1995-02-28 ES ES95400426T patent/ES2146294T3/es not_active Expired - Lifetime
Patent Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0212157A2 (fr) * | 1985-08-20 | 1987-03-04 | VARTA Batterie Aktiengesellschaft | Dispositif de coulée de grillages de plomb pour plaques d'accumulateurs et procédé pour sa fabrication |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101456061B (zh) * | 2007-12-10 | 2010-08-11 | 洛阳双瑞精铸钛业有限公司 | 一种提高石墨型钛合金铸件质量的辅助工艺 |
Also Published As
| Publication number | Publication date |
|---|---|
| DE69516566T2 (de) | 2001-02-08 |
| FR2716898B1 (fr) | 1996-06-07 |
| DE69516566D1 (de) | 2000-06-08 |
| FR2716898A1 (fr) | 1995-09-08 |
| EP0670190A1 (fr) | 1995-09-06 |
| ES2146294T3 (es) | 2000-08-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4705203A (en) | Repair of surface defects in superalloy articles | |
| US6702886B2 (en) | Mold coating | |
| JP2009541201A (ja) | 白金族金属または白金族金属合金被覆を有する耐火性金属酸化物セラミック部材 | |
| CH661287A5 (fr) | Procede de preparation par diffusion d'une couche protectrice sur des alliages a base de nickel, cobalt et fer. | |
| JPS648072B2 (fr) | ||
| FR2685227A1 (fr) | Amelioration de l'aptitude au travail a chaud par utilisation de revetement depose par projection thermique. | |
| WO2003037823A1 (fr) | Procede de metallisation et/ou de brasage par un alliage de silicium de pieces en ceramique oxyde non mouillable par ledit alliage | |
| JPS6350402B2 (fr) | ||
| EP0670190A1 (fr) | Moule de fonderie et son procédé de réalisation | |
| KR101862526B1 (ko) | 다이캐스트용 피복 금형의 제조 방법 | |
| EP0578518A1 (fr) | Procédé de formation d'un insert sur une pièce à revêtir en acier ou en alliage de titane | |
| EP1846588B1 (fr) | Procédé d'élaboration par projection thermique d'une cible à base de silicium et de zirconium | |
| KR100847911B1 (ko) | 주조기계 부품용 금속재료 및 알루미늄 용탕 접촉부재와 그제조방법 | |
| WO2022254139A1 (fr) | Procede de revetement d'une piece en alliage refractaire et piece ainsi revetue | |
| JP2004314170A (ja) | アルミニウム又はアルミニウム合金から成るストリップを鋳造するための鋳造ロール | |
| CN107900309A (zh) | 一种表面双层结构压铸模具及其制备方法 | |
| JPS6362858A (ja) | セラミツク溶射層の形成方法 | |
| JP4604640B2 (ja) | 真空装置用部品及びその製造方法並びにそれを用いた装置 | |
| JP2003170262A (ja) | ダイカストマシン用部材の製造方法 | |
| WO2020030880A1 (fr) | Revetement pour piece en alliage refractaire | |
| US20170283973A1 (en) | Metallurgically bonded wear resistant texture coatings for aluminum alloys and metal matrix composite electrode for producing same | |
| JPH11158599A (ja) | 断熱層及びその製造方法 | |
| US8283047B2 (en) | Method of making composite casting and composite casting | |
| JP7174949B2 (ja) | チタン製器具の製造方法 | |
| FR2736850A1 (fr) | Moule de fonderie et procede de realisation d'un tel moule |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE ES GB IT |
|
| 17P | Request for examination filed |
Effective date: 19951002 |
|
| 17Q | First examination report despatched |
Effective date: 19980317 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE ES GB IT |
|
| REF | Corresponds to: |
Ref document number: 69516566 Country of ref document: DE Date of ref document: 20000608 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20000525 |
|
| ITF | It: translation for a ep patent filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2146294 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20060228 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20070130 Year of fee payment: 13 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20070131 Year of fee payment: 13 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 746 Effective date: 20070115 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20070209 Year of fee payment: 13 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20080228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080902 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20080229 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20080229 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20070228 |