EP0678338A1 - Vorrichtung zur Beschichtung von Bahnmaterial - Google Patents
Vorrichtung zur Beschichtung von Bahnmaterial Download PDFInfo
- Publication number
- EP0678338A1 EP0678338A1 EP95201006A EP95201006A EP0678338A1 EP 0678338 A1 EP0678338 A1 EP 0678338A1 EP 95201006 A EP95201006 A EP 95201006A EP 95201006 A EP95201006 A EP 95201006A EP 0678338 A1 EP0678338 A1 EP 0678338A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- roll
- application roll
- substrate web
- counterpressure
- application
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images
Classifications
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21H—PULP COMPOSITIONS; PREPARATION THEREOF NOT COVERED BY SUBCLASSES D21C OR D21D; IMPREGNATING OR COATING OF PAPER; TREATMENT OF FINISHED PAPER NOT COVERED BY CLASS B31 OR SUBCLASS D21G; PAPER NOT OTHERWISE PROVIDED FOR
- D21H23/00—Processes or apparatus for adding material to the pulp or to the paper
- D21H23/02—Processes or apparatus for adding material to the pulp or to the paper characterised by the manner in which substances are added
- D21H23/22—Addition to the formed paper
- D21H23/52—Addition to the formed paper by contacting paper with a device carrying the material
- D21H23/56—Rolls
- D21H23/58—Details thereof, e.g. surface characteristics, peripheral speed
- D21H23/62—Reverse roll coating, i.e. applicator roll surface moving in direction opposite to that of the paper
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C—APPARATUS FOR APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05C1/00—Apparatus in which liquid or other fluent material is applied to the surface of the work by contact with a member carrying the liquid or other fluent material, e.g. a porous member loaded with a liquid to be applied as a coating
- B05C1/04—Apparatus in which liquid or other fluent material is applied to the surface of the work by contact with a member carrying the liquid or other fluent material, e.g. a porous member loaded with a liquid to be applied as a coating for applying liquid or other fluent material to work of indefinite length
- B05C1/08—Apparatus in which liquid or other fluent material is applied to the surface of the work by contact with a member carrying the liquid or other fluent material, e.g. a porous member loaded with a liquid to be applied as a coating for applying liquid or other fluent material to work of indefinite length using a roller or other rotating member which contacts the work along a generating line
- B05C1/0826—Apparatus in which liquid or other fluent material is applied to the surface of the work by contact with a member carrying the liquid or other fluent material, e.g. a porous member loaded with a liquid to be applied as a coating for applying liquid or other fluent material to work of indefinite length using a roller or other rotating member which contacts the work along a generating line the work being a web or sheets
- B05C1/0834—Apparatus in which liquid or other fluent material is applied to the surface of the work by contact with a member carrying the liquid or other fluent material, e.g. a porous member loaded with a liquid to be applied as a coating for applying liquid or other fluent material to work of indefinite length using a roller or other rotating member which contacts the work along a generating line the work being a web or sheets the coating roller co-operating with other rollers, e.g. dosing, transfer rollers
Definitions
- the invention relates to a device for applying a coating layer to a substrate web, comprising an application roll for applying the coating layer to the substrate web, a counterpressure roll interacting with the application roll in order to support a substrate web passing through between the application roll and the counterpressure roll, and a metering device for applying a coating material in a layer to the application roll, the application roll being designed to rotate in the same direction as the counterpressure roll, so that at the position of the counterpressure roll the direction of movement of the periphery of the application roll is opposite to that of the counterpressure roll.
- Such devices are known and are called reverse-roll coaters. Two types of devices can be distinguished here, depending on the type of metering device which is used.
- the metering device In the case of the first type the metering device consists of a metering roll which interacts with the application roll. The metering roll runs through a bath of the coating material and takes up this material in the process. The material taken up is then transferred to the application roll.
- This type of device is suitable in particular for applying coating materials of relatively low viscosity.
- the disadvantage of the device is that the quantity of coating material taken up from the bath cannot be regulated well. Additional measures are necessary to regulate the quantity of coating material on the application roll, for example using a scraper knife.
- the metering device also consists of a metering roll interacting with the application roll. Said metering device is situated a short distance away from the application roll.
- the relatively highly viscous coating material lies in the channel formed by the metering roll and application roll, and is taken up through the gap between the application roll and the metering roll.
- the disadvantage of this type of device is that the quantity of coating material on the application roll depends on the distance between the metering roll and the application roll. When substrate webs of great width (for example, 3 to 4 metres) are being coated, the accuracy and the stability of the metering roll and application roll need to be high over the full width in order to obtain a uniform thickness of coating layer.
- the object of the invention is to provide a device for the application of a coating layer to a substrate web, in which the disadvantages of the known devices are overcome.
- the metering device comprises a rotating cylindrical screen and supply means for supplying the coating material.
- the device according to the invention it is possible to regulate the thickness of the coating layer within very narrow limits, so that very low layer thicknesses, corresponding to a quantity of coating material of 5 - 6 grammes per m2 can be achieved.
- the thickness of the coating layer can be regulated easily by the choice of type of screen and the speed of the application roll relative to the counterpressure roll.
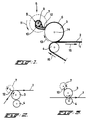
- Fig. 1 shows diagrammatically the layout of a device for applying the coating layer to a substrate web.
- the substrate web is indicated by the reference number 1 and the coating layer by the reference number 2.
- the device comprises an application roll 3 for applying the coating layer 2 to the substrate web 1, a counterpressure roll 4 interacting with the application roll 3 in order to support the substrate web 1 passing through between the application roll 3 and the counterpressure roll 4, and also a metering device 5 for applying the coating material in a layer 6 to the application roll 3.
- the metering device 5 consists of a rotating cylindrical screen 7 and a squeegee 8, preferably of the closed type, disposed inside the screen.
- a squeegee 8 preferably of the closed type, disposed inside the screen.
- other types of squeegees such as open-type squeegees, roller squeegees etc., can also be used.
- the device operates as follows.
- the coating material 9 is supplied through the inside of the squeegee 8.
- the coating material 9 flows through a gap 10, extending in the lengthwise direction of the squeegee 8, into the inside of the cylindrical screen 7.
- the screen 7 rotates in the direction of the arrow 11.
- the coating material is forced through the screen and thus applied in a layer 6 to the outside of the application roll 3, which rotates in the direction of the arrow 13.
- the free edge of the squeegee blade 12 preferably lies in the plane through the axis of the rotating screen 7 and the axis 14 of the application roll 3. Very good metering of the coating material can be achieved in this way.
- the coating material is then applied by the application roll 3 to the substrate web 1, which is passed around the counterpressure roll 4 and runs through between the application roll 3 and the counterpressure roll 4 in the direction of the arrows 15.
- Such a type of device is therefore often known as a reverse-roll coater.
- the application roll 3, at least at the periphery, is made of a shape-retaining (hard) material, i.e. a material which is shape-retaining under the loads occurring upon the roll.
- the shape-retaining material used is, for example, metal or ceramic material.
- the counterpressure roll 4 at least at the periphery, is made of a resilient material, i.e. a material which can eliminate slight unevennesses in the substrate web to be coated and slight deviations in the parallelism of the application roll 3 and the counterpressure roll 4. Moreover, the coefficient of friction of the resilient material of the counterpressure roll 4 should be greater than that of the shape-retaining material of the application roll 3, so that the substrate web to be coated is conveyed through the counterpressure roll 4.
- the resilient material used is, for example, rubber.
- the gap between the application roll 3 and the counterpressure roll 4 is preferably slightly smaller than the thickness of the substrate web to be coated.
- the thickness of the coating layer 2 can be regulated by means of three parameters: the type of screen (mesh, thickness and open area) , the squeegee pressure and the speed of the application roll 3 relative to the counterpressure roll 4, and thus the substrate web 1.
- a low weight of coating material can be applied to the application roll 3 by selecting a screen with a high mesh number (many holes), in conjunction with a low wall thickness and a relatively small open area. The reverse applies to a screen with a low mesh number (fewer holes), a greater wall thickness and a large open area.
- the squeegee pressure i.e. the pressure of the squeegee blade 12 against the screen 7 also plays a role.
- the thickness of the coating layer 2 can also be regulated by regulating the speed of the application roll 3 relative to the speed of the substrate web 1. The higher the speed of the application roll 3 relative to the speed of the substrate web 1, the thicker will be the coating layer 2.
- the device according to the invention can also be used more generally, for example for direct screen printing and indirect screen printing.
- the substrate web 1 is passed through between the rotating screen 7 and the application roll 3, as shown diagrammatically in Fig. 2, and a pattern is printed on the substrate web.
- the diameter of the cylindrical screen 7 is preferably the same as the diameter of the application roll 3, and provision is made for drive means by which the cylindrical screen 7 and the application roll 3 can be driven in such a way that they rotate at the same peripheral speed, but in opposite directions of rotation.
- the device according to the invention is therefore such that it can be used for several purposes, possibly with minor adjustments.
Landscapes
- Coating Apparatus (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| NL9400646A NL9400646A (nl) | 1994-04-22 | 1994-04-22 | Inrichting voor het aanbrengen van een bekledingslaag op een substraatbaan. |
| NL9400646 | 1994-04-22 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP0678338A1 true EP0678338A1 (de) | 1995-10-25 |
Family
ID=19864099
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP95201006A Withdrawn EP0678338A1 (de) | 1994-04-22 | 1995-04-20 | Vorrichtung zur Beschichtung von Bahnmaterial |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0678338A1 (de) |
| JP (1) | JPH07299400A (de) |
| NL (1) | NL9400646A (de) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114775963A (zh) * | 2022-05-25 | 2022-07-22 | 深圳市卓宝科技股份有限公司 | 一种防水涂料施工方法和实施该方法的铺设装置 |
Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3511696A (en) * | 1966-06-16 | 1970-05-12 | Stauffer Chem Co Of Canada Ltd | Reverse roll coating process and apparatus |
| EP0095819A2 (de) * | 1982-06-02 | 1983-12-07 | Stork Brabant B.V. | Druckapparat, insbesondere für das Aufbringen von Lack |
-
1994
- 1994-04-22 NL NL9400646A patent/NL9400646A/nl not_active Application Discontinuation
-
1995
- 1995-04-20 JP JP9492895A patent/JPH07299400A/ja not_active Withdrawn
- 1995-04-20 EP EP95201006A patent/EP0678338A1/de not_active Withdrawn
Patent Citations (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3511696A (en) * | 1966-06-16 | 1970-05-12 | Stauffer Chem Co Of Canada Ltd | Reverse roll coating process and apparatus |
| EP0095819A2 (de) * | 1982-06-02 | 1983-12-07 | Stork Brabant B.V. | Druckapparat, insbesondere für das Aufbringen von Lack |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114775963A (zh) * | 2022-05-25 | 2022-07-22 | 深圳市卓宝科技股份有限公司 | 一种防水涂料施工方法和实施该方法的铺设装置 |
Also Published As
| Publication number | Publication date |
|---|---|
| JPH07299400A (ja) | 1995-11-14 |
| NL9400646A (nl) | 1995-12-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4442144A (en) | Method for forming a coating on a substrate | |
| US4357370A (en) | Twin short dwell coater arrangement | |
| EP0003790B1 (de) | Vorrichtung zum Beschichten einer sich bewegenden Bahn | |
| KR970020215A (ko) | 재료 표면에 점성 액체를 도포하기 위한 장치 및 방법 | |
| US4822640A (en) | Coater | |
| US3511696A (en) | Reverse roll coating process and apparatus | |
| US3951102A (en) | Roller coating apparatus | |
| GB2046133A (en) | Apparatus for applying foam to a moving web | |
| US4347269A (en) | Method of and apparatus for applying a coating to a web of sheet material | |
| US5795386A (en) | Apparatus for applying a coating layer to a substrate web | |
| JP2889128B2 (ja) | 塗布方法及びその装置 | |
| CA1247469A (en) | Carpet coating method and apparatus | |
| FI66448C (fi) | Belaeggningsanordning foer bana | |
| JP3010068B2 (ja) | コーティング方法 | |
| GB2171934A (en) | Two-sided coating of paper webs | |
| GB1571946A (en) | Process and device for coating a film | |
| US2534321A (en) | Coating method and apparatus | |
| US4363288A (en) | Device for applying a coating layer to a strip of continuously moving material | |
| EP0848110B1 (de) | Auftragskopf mit Formung der Klinge | |
| US5738724A (en) | Actuator assembly for coater blade load adjustment | |
| US6444270B1 (en) | Photo film coating method for coating web-shaped base material | |
| US5782976A (en) | Continuous coater blade | |
| JPH10244191A (ja) | 接着剤塗布装置 | |
| JP2584923Y2 (ja) | 塗工装置 | |
| NL9400646A (nl) | Inrichting voor het aanbrengen van een bekledingslaag op een substraatbaan. |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE FR GB IT NL |
|
| 17P | Request for examination filed |
Effective date: 19960425 |
|
| 17Q | First examination report despatched |
Effective date: 19980527 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: STORK BRABANT B.V. |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20000321 |