EP0767253A1 - Appareil de revêtement en continu par immersion d'une bande d'acier - Google Patents
Appareil de revêtement en continu par immersion d'une bande d'acier Download PDFInfo
- Publication number
- EP0767253A1 EP0767253A1 EP95115689A EP95115689A EP0767253A1 EP 0767253 A1 EP0767253 A1 EP 0767253A1 EP 95115689 A EP95115689 A EP 95115689A EP 95115689 A EP95115689 A EP 95115689A EP 0767253 A1 EP0767253 A1 EP 0767253A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- steel strip
- rollers
- deflection
- deflecting
- roller
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 229910000831 Steel Inorganic materials 0.000 title claims abstract description 20
- 239000010959 steel Substances 0.000 title claims abstract description 20
- 238000007598 dipping method Methods 0.000 title 1
- 239000011261 inert gas Substances 0.000 claims abstract description 7
- 238000001465 metallisation Methods 0.000 claims description 2
- 239000011248 coating agent Substances 0.000 description 5
- 238000000576 coating method Methods 0.000 description 5
- 230000000694 effects Effects 0.000 description 5
- 229910045601 alloy Inorganic materials 0.000 description 4
- 239000000956 alloy Substances 0.000 description 4
- 229910001338 liquidmetal Inorganic materials 0.000 description 3
- IJGRMHOSHXDMSA-UHFFFAOYSA-N Atomic nitrogen Chemical compound N#N IJGRMHOSHXDMSA-UHFFFAOYSA-N 0.000 description 2
- 238000004140 cleaning Methods 0.000 description 2
- 230000002349 favourable effect Effects 0.000 description 2
- 239000007788 liquid Substances 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 229910052751 metal Inorganic materials 0.000 description 2
- 239000002184 metal Substances 0.000 description 2
- 238000007790 scraping Methods 0.000 description 2
- 230000015572 biosynthetic process Effects 0.000 description 1
- 238000006243 chemical reaction Methods 0.000 description 1
- 239000010960 cold rolled steel Substances 0.000 description 1
- 239000000470 constituent Substances 0.000 description 1
- 238000006073 displacement reaction Methods 0.000 description 1
- -1 ferrous metals Chemical class 0.000 description 1
- 229910052757 nitrogen Inorganic materials 0.000 description 1
- 238000010408 sweeping Methods 0.000 description 1
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C2/00—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor
- C23C2/34—Hot-dipping or immersion processes for applying the coating material in the molten state without affecting the shape; Apparatus therefor characterised by the shape of the material to be treated
- C23C2/36—Elongated material
- C23C2/40—Plates; Strips
Definitions
- the invention relates to a device for the continuous hot dip metallization of a steel strip.
- the known deflection rollers have a wrap angle for the steel belt of at least 120 °, which results in a very large contact area between the roller and the belt.
- this large contact area is very unfavorable, since it traps liquid parts of the alloy bath between the belt and the roller. This in turn leads to strip deformations which reduce quality, since the liquid, trapped metal cannot escape and the sheet steel strip is guided with great tension over the deflection rollers.
- a large wrap angle on the deflecting roller also has the result that, due to the large roller surface, a large amount of deposits can build up, which arise as a result of reactions of aggressive constituents of the alloy bath with the roller surface, which in turn leave marks and grooves in the surface of the surface to be coated Cause steel strip, which lowers its quality.
- the invention has for its object to develop a device of the type described above so that the product quality of the coated steel strip is improved.
- the device has at least two deflecting rollers for deflecting the steel strip, each deflecting roller having a mechanical scraper provided with an inert gas supply for removing deposits.
- each individual deflecting roller can be made smaller than when using only a single deflecting roller. If the belt speed remains unchanged, this increases the angular speed of the individual deflecting rollers, so that the scraping result improves due to the greater frequency of passage of each individual surface element of the roller. Due to the distribution of the total wrap angle of at least 120 ° over several individual deflecting rollers, there are smaller individual wrap angles, which reduces the risk of deformation and markings on the belt due to the inclusion of liquid metal between the roll surface and the steel belt.
- the coating quality of steel strips can be increased considerably if a mechanical scraper is attached to each individual deflecting roller and is connected to an inert gas supply. Compared to a single large deflection roller, the scraper effectiveness is significantly increased, which results in a significant increase in material quality and an increase in the service life of both the deflection rollers and the scraper.
- This configuration is distinguished by very particularly favorable results with regard to the product quality and the service life of the deflecting rollers and the scrapers, with a particularly favorable ratio between the investment costs of the device and the achievable product quality.
- At least two tensioning rollers are provided in addition to the deflection rollers.
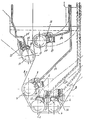
- a steel strip B which moves in the direction of arrow A through a molten coating bath, is deflected by three deflecting rollers 1, 2 and 3 with respect to its original direction of movement by approximately 180 °, all three deflecting rollers having the same diameter.
- Scraper holder boxes 4, 5 and 6 are arranged on the sides of the deflecting rollers 1, 2 and 3 facing away from the steel strip B, which are each provided with articulated scrapers 7, 8 and 9.
- the steel strip B is guided over two tensioning rollers 10 and 11, which are mounted on parallel axes.
- the tensioning rollers 10 and 11 are also provided with scraper holder boxes 12 and 13 in which articulated scraper 14 and 15 are arranged.
- the scrapers 7, 8, 9, 14 and 15 are provided with cutting edges 16, 17, 18, 19 and 20 which sweep over the surface of the respective roller and thus prevent deposits from sticking to the rollers or remove deposits which have already formed .
- each of the scraper holder boxes 4, 5, 6, 12 and 13 ends an inert gas supply 21 to 25, through which in the scraper holder boxes 4, 5, 6, 12 and 13 e.g. Nitrogen is supplied as an inert gas, whereby the cleaning effect of the cutting edges 16 to 20 is significantly improved.
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Coating With Molten Metal (AREA)
- Coating Apparatus (AREA)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP95115689A EP0767253A1 (fr) | 1995-10-05 | 1995-10-05 | Appareil de revêtement en continu par immersion d'une bande d'acier |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP95115689A EP0767253A1 (fr) | 1995-10-05 | 1995-10-05 | Appareil de revêtement en continu par immersion d'une bande d'acier |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP0767253A1 true EP0767253A1 (fr) | 1997-04-09 |
Family
ID=8219684
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP95115689A Withdrawn EP0767253A1 (fr) | 1995-10-05 | 1995-10-05 | Appareil de revêtement en continu par immersion d'une bande d'acier |
Country Status (1)
| Country | Link |
|---|---|
| EP (1) | EP0767253A1 (fr) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1134301A1 (fr) * | 2000-03-16 | 2001-09-19 | Kawasaki Steel Corporation | Lame de rouleau immergé pour bain de galvanisation et procédé pour empêcher la formation de défauts |
| CN109023194A (zh) * | 2018-08-24 | 2018-12-18 | 合肥集知网信息技术有限公司 | 一种单面镀锌钢板表面处理工艺 |
| WO2021161923A1 (fr) * | 2020-02-12 | 2021-08-19 | 日本製鉄株式会社 | Dispositif d'aide à la détermination de l'état de surface d'un rouleau, dispositif d'élimination de substances étrangères sur la surface d'un rouleau et procédé d'élimination de substances étrangères sur la surface d'un rouleau |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2293840A (en) * | 1939-07-13 | 1942-08-25 | Gen Motors Corp | Impregnating apparatus |
| FR1316835A (fr) * | 1961-03-03 | 1963-02-01 | Vitkovice Zelezarny | Dispositif pour l'essuyage du métal liquide en excès de la surface des cylindres de travail pour le reve6tement métallique de tôles et bandes d'acier |
| FR1424879A (fr) * | 1965-02-17 | 1966-01-14 | British Insulated Callenders | Procédés et appareils perfectionnés destinés à enduire des fils, metalliques avec du métal |
| DE2610632B1 (de) * | 1976-03-13 | 1977-09-01 | Wilhelm Mueschen | Verwendung eines keil- oder kurvenfoermig gestalteten abstreifers in zink-, blei-, zinn- oder aluminium-schmelzbaedern |
| JPS61133369A (ja) * | 1984-11-30 | 1986-06-20 | Kawatetsu Kohan Kk | 溶融金属メツキ浴中ロ−ルの表面付着物の除去方法 |
| JPH1142068A (ja) * | 1997-07-29 | 1999-02-16 | Nisshin Flour Milling Co Ltd | 中華饅頭の製造方法 |
-
1995
- 1995-10-05 EP EP95115689A patent/EP0767253A1/fr not_active Withdrawn
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2293840A (en) * | 1939-07-13 | 1942-08-25 | Gen Motors Corp | Impregnating apparatus |
| FR1316835A (fr) * | 1961-03-03 | 1963-02-01 | Vitkovice Zelezarny | Dispositif pour l'essuyage du métal liquide en excès de la surface des cylindres de travail pour le reve6tement métallique de tôles et bandes d'acier |
| FR1424879A (fr) * | 1965-02-17 | 1966-01-14 | British Insulated Callenders | Procédés et appareils perfectionnés destinés à enduire des fils, metalliques avec du métal |
| DE2610632B1 (de) * | 1976-03-13 | 1977-09-01 | Wilhelm Mueschen | Verwendung eines keil- oder kurvenfoermig gestalteten abstreifers in zink-, blei-, zinn- oder aluminium-schmelzbaedern |
| JPS61133369A (ja) * | 1984-11-30 | 1986-06-20 | Kawatetsu Kohan Kk | 溶融金属メツキ浴中ロ−ルの表面付着物の除去方法 |
| JPH1142068A (ja) * | 1997-07-29 | 1999-02-16 | Nisshin Flour Milling Co Ltd | 中華饅頭の製造方法 |
Non-Patent Citations (3)
| Title |
|---|
| PATENT ABSTRACTS OF JAPAN vol. 10, no. 328 (C - 383) 7 November 1986 (1986-11-07) * |
| PATENT ABSTRACTS OF JAPAN vol. 13, no. 399 (C - 632) 5 September 1989 (1989-09-05) * |
| PATENT ABSTRACTS OF JAPAN vol. 16, no. 144 (C - 0927) 10 April 1992 (1992-04-10) * |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1134301A1 (fr) * | 2000-03-16 | 2001-09-19 | Kawasaki Steel Corporation | Lame de rouleau immergé pour bain de galvanisation et procédé pour empêcher la formation de défauts |
| US6485570B2 (en) | 2000-03-16 | 2002-11-26 | Kawasaki Steel Corporation | Sink roll blade apparatus used in continuous molten metal plating apparatus and method for preventing occurrence of dents |
| CN109023194A (zh) * | 2018-08-24 | 2018-12-18 | 合肥集知网信息技术有限公司 | 一种单面镀锌钢板表面处理工艺 |
| WO2021161923A1 (fr) * | 2020-02-12 | 2021-08-19 | 日本製鉄株式会社 | Dispositif d'aide à la détermination de l'état de surface d'un rouleau, dispositif d'élimination de substances étrangères sur la surface d'un rouleau et procédé d'élimination de substances étrangères sur la surface d'un rouleau |
| JPWO2021161923A1 (fr) * | 2020-02-12 | 2021-08-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE2746238C2 (de) | Vorrichtung zum Stranggießen eines dünnen Metallstreifens | |
| DE2901896C2 (de) | Vorrichtung zur Entzunderung von Blechband od.dgl. | |
| DE2054999A1 (de) | Verfahren zum Einstellen eines Überzuges und Vorrichtung zur Durch fuhrung des Verfahrens | |
| DE112006004168T5 (de) | Gasabstreifvorrichtung mit Vielfachdüsen | |
| DE69415771T2 (de) | Vorrichtung zum Entfernen von auf Bandrändern befindlichen Flüssigkeitsansammelungen | |
| DE2728741A1 (de) | Einrichtung zum auftragen einer schutzschicht auf die schweissnaht von dosenruempfen | |
| EP2776600A1 (fr) | Procédé et dispositif de revêtement au trempé d'un feuillard métallique avec un revêtement métallique | |
| DE69323214T2 (de) | Vorrichtung und verfahren zur minimierung von beschichtungslücken auf einer papierbahn | |
| EP1900449A1 (fr) | Poutre de pulvérisation d'une installation de décalaminage hydraulique et procédé de fonctionnement d'une telle poutre de pulvérisation | |
| DE68906486T2 (de) | Abstreifdüse. | |
| DE3435501C2 (de) | Vorrichtung zum kontinuierlichen Kühlen einer erwärmten, waagerecht liegenden Metallplatte | |
| EP0695590A1 (fr) | Procédé et dispositif de refroidissement des tÔles et des bandes laminées à chaud | |
| DE2310526C2 (de) | Vorrichtung zum beidseitigen Aufbringen eines Striches aus unterschiedlicher Bestreichmasse auf eine bewegte Papierbahn | |
| DE69310804T2 (de) | Abstreifen von flüssigen Beschichtungen | |
| DE19517256C2 (de) | Vorrichtung zur kontinuierlichen Heißtauchmetallisierung eines Stahlbandes | |
| DE3040503C2 (fr) | ||
| EP0054172B1 (fr) | Procédé et installation pour le laminage d'une bande détensionnée | |
| DE3150946A1 (de) | "vorrichtung zum entzundern eines stahlstrangs" | |
| DE3048672C2 (fr) | ||
| DE2819142A1 (de) | Verfahren und vorrichtung zum einseitigen beschichten eines metallbandes mit schmelzfluessigem metall, insbesondere zum einseitigen feuerverzinken von stahlband | |
| EP1201037B1 (fr) | Procede et dispositif pour refroidir un feuillard metallique | |
| DE10234109A1 (de) | Verfahren und Vorrichtung zur kontinuierlichen Herstellung metallischer Bänder | |
| DE3526060A1 (de) | Vorrichtung zum aufteilen eines produktstromes aus druckexemplaren in mehrere auslegestationen | |
| EP0188813A2 (fr) | Procédé et appareil pour étaler un revêtement liquide sur une bande, en particulier revêtement par immersion à chaud d'une bande de métal ferreux | |
| AT369436B (de) | Verfahren zum kontinuierlichen einseitigen beschichten eines blanken metallbandes mit geschmolzenem metall sowie vorrichtung zur durch- fuehrung des verfahrens |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE DE ES FR GB IT LU NL SE |
|
| 17P | Request for examination filed |
Effective date: 19970421 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 19990519 |