EP0776703B1 - Vorrichtung zum elektrostatischen Pulverbeschichten der Oberfläche eines Bandes - Google Patents
Vorrichtung zum elektrostatischen Pulverbeschichten der Oberfläche eines Bandes Download PDFInfo
- Publication number
- EP0776703B1 EP0776703B1 EP96116810A EP96116810A EP0776703B1 EP 0776703 B1 EP0776703 B1 EP 0776703B1 EP 96116810 A EP96116810 A EP 96116810A EP 96116810 A EP96116810 A EP 96116810A EP 0776703 B1 EP0776703 B1 EP 0776703B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- band
- powder
- coating
- arrangement according
- coated
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B05—SPRAYING OR ATOMISING IN GENERAL; APPLYING FLUENT MATERIALS TO SURFACES, IN GENERAL
- B05B—SPRAYING APPARATUS; ATOMISING APPARATUS; NOZZLES
- B05B5/00—Electrostatic spraying apparatus; Spraying apparatus with means for charging the spray electrically; Apparatus for spraying liquids or other fluent materials by other electric means
- B05B5/08—Plant for applying liquids or other fluent materials to objects
- B05B5/14—Plant for applying liquids or other fluent materials to objects specially adapted for coating continuously moving elongated bodies, e.g. wires, strips, pipes
Definitions
- the invention relates to a device for electrostatic Powder coating the surface of an electrostatic tape chargeable material, especially metal, that runs lengthways a coating line continuously on a coating device is led past.
- a metal band is common in powder coating technology from a coil of strip metal in a continuous Process, pre-treat, coat with powder, burn the powder and the one side coated Rewinding the metal strip or processing it directly.
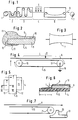
- Fig. 1 This is shown in Fig. 1, where with the reference number 1 Raw metal roll ("raw coil"), with reference number 2 a pretreatment bath, a dryer with reference number 3, a dryer with reference number 4 Coating line, with reference number 5 a coating device with powder spray nozzles on the front of the to be coated Metal strip, with reference number 6 a baking oven and with reference number 7 a take-up roll for the finished coated Metal tape are labeled.
- Raw metal roll (“raw coil")
- reference number 2 a pretreatment bath
- a dryer with reference number 3 a dryer with reference number 4 Coating line
- reference number 5 a coating device with powder spray nozzles on the front of the to be coated Metal strip
- reference number 6 a baking oven and with reference number 7 a take-up roll for the finished coated Metal tape are labeled.
- the metal strip itself is identified by the reference number 8, and in Fig. 2 is in a partial cross section on a larger scale a side edge of the metal strip 8 shown that after the Leaving the baking oven 6 on its front 9 with one baked powder layer 10 is covered. Due to the increased field strengths developing at the side edges electrostatic powder coating forms on them Side edges of a thickened bead 11, the side edge 12 engages so that the back 14 of the metal strip 8th is coated with powder in the edge region at 13. If so finished coated metal strip 8 after baking on the Winding roll 7 wound, so the effect increases edge thickening due to the large number of coils Lay to the side edges of the take-up reel 7, and it forms a concave tape roll 7 as shown in FIG. 3, in which the Did not lie evenly on top of each other across the width of the roll lie. If the edge thickening on the two side edges and on roller 7 is not absolutely the same, it even results a roll of tape wound wrong.
- German patent DE 26 60 293 C2 is a metal substrate known that a lubricant application on a surface having by electrostatic application of Lubricant particles was formed, as well as a method for Production of such an electrostatically chargeable metal substrate.
- this metal substrate becomes longitudinal a coating line continuously on a coating device passed by. Thereby lie on the back of the metal substrate with these moving, endless treadmills on.
- the invention has for its object a device type described above so that a bulge-like thickening of the band on the side edges avoided and a uniformly thick coating only the Surface on the front of the tape over its entire Width is ensured.
- the treadmill lies against the lower surface of the metal belt and is preferably at the same speed as that to be coated Band moves. Because of the preferably on both Sides of the same protrusion of the treadmill compared to the one above arranged metal tape takes the powder electrostatically no longer true band edge but just a step that everywhere has the same (earth) potential.
- the Thickness of the strip to be coated is small compared to the protrusions on both sides, and if the distance of electrostatic Coating device (powder spray nozzles) also greater than the level, this level can be electrostatic be neglected, so that on the side edges of the metal strip no or at most a greatly reduced bead formation occurs. In addition, it is certainly prevented that powder on the Reaches the bottom surface of the metal strip.
- the invention is preferred for a device for continuous Coating one from a roll of raw tape ("Rohcoil”) unwound metal tape applied.
- the treadmill is advantageously endless and overflows Roll around, one of which is powered.
- the preferred straight coating line of the metal strip runs horizontally or vertically.
- the coating device comprises Powder spray nozzles whose spray direction is vertical or better aligned obliquely in the running direction of the strip to be coated is, as is known in itself. With an oblique spray direction the relative speed of the powder particles to the belt is small, so that the electrostatic attractive forces work better can. This allows higher belt speeds.
- the treadmill is preferably one at its trailing end Powder suction device assigned so that even in this area a bulge of the powder layer on the side edges can be avoided.
- the suctioned powder can circulate can be fed again so that no powder loss occurs. Rather, when using a device the invention because of avoiding the formation of beads on the side Edges of powder saved.
- FIG. 4 shows the part of a device according to FIG. 1 in the area a horizontal coating section 4, below the metal belt 8 an endless treadmill 15 made of electrical conductive material over rollers 16, 17 at the same speed how the speed of the metal strip 8 moves becomes.
- One of the two rollers 16, 17 is driven, and the treadmill 15 is grounded via the roller 17 at 18.
- the top of the treadmill 15 lies on the back 14 of the metal belt 8 as shown in FIG. 6.
- the ratio between the thickness t to the protrusion s should be in in practice are between 1/1000 and 1/30. Practical values for the thickness t of the tape and the size of the overhang s are for thickness t: 0.5 - 3 mm, for the projection s: 9 - 50 cm and for the bandwidth b: 1cm - 2m.
- the belt speed can be 10 - 50 m / min.
- the thickness of the powder layer In practice 10 is 20 - 60 ⁇ m.
- Metal strips 8 to be coated can be found on the back pretreatment with a very thin roller-applied UV-hardened wet lacquer film as scratch protection have been (not shown in Fig. 1). To the Do not scratch the back 14, should the treadmill 15 be relatively soft. For this reason it is preferred if that Treadmill 15 a conductive coated (plastic) fabric belt is.
Landscapes
- Application Of Or Painting With Fluid Materials (AREA)
- Electrostatic Spraying Apparatus (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19544530 | 1995-11-29 | ||
| DE19544530A DE19544530C1 (de) | 1995-11-29 | 1995-11-29 | Vorrichtung zum elektrostatischen Pulverbeschichten der Vorderseite eines Bandes |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0776703A1 EP0776703A1 (de) | 1997-06-04 |
| EP0776703B1 true EP0776703B1 (de) | 1999-06-30 |
Family
ID=7778726
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP96116810A Expired - Lifetime EP0776703B1 (de) | 1995-11-29 | 1996-10-18 | Vorrichtung zum elektrostatischen Pulverbeschichten der Oberfläche eines Bandes |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0776703B1 (da) |
| AT (1) | ATE181681T1 (da) |
| DE (2) | DE19544530C1 (da) |
| DK (1) | DK0776703T3 (da) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP3817393B2 (ja) * | 1999-08-12 | 2006-09-06 | 株式会社メサック | 静電植毛並に静電塗装を施す静電加工室 |
| JP3825588B2 (ja) * | 1999-08-23 | 2006-09-27 | 住友商事株式会社 | 静電植毛装置、静電塗装装置に配する静電加工室 |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3776187A (en) * | 1970-08-05 | 1973-12-04 | Ransburg Electro Coating Corp | Electrostatic deposition apparatus |
| US3874333A (en) * | 1972-09-28 | 1975-04-01 | Nat Steel Corp | Preventing edge wrap-around in one-side electrostatic coating |
| GB1549711A (en) * | 1975-04-22 | 1979-08-08 | Ball Corp | Apparatus for applying lubricating materials to substrates |
| JPS644272A (en) * | 1987-06-24 | 1989-01-09 | Hideo Nagasaka | Electrostatic powder coating device |
-
1995
- 1995-11-29 DE DE19544530A patent/DE19544530C1/de not_active Expired - Fee Related
-
1996
- 1996-10-18 DE DE59602327T patent/DE59602327D1/de not_active Expired - Fee Related
- 1996-10-18 DK DK96116810T patent/DK0776703T3/da active
- 1996-10-18 EP EP96116810A patent/EP0776703B1/de not_active Expired - Lifetime
- 1996-10-18 AT AT96116810T patent/ATE181681T1/de not_active IP Right Cessation
Also Published As
| Publication number | Publication date |
|---|---|
| ATE181681T1 (de) | 1999-07-15 |
| DK0776703T3 (da) | 1999-11-22 |
| EP0776703A1 (de) | 1997-06-04 |
| DE19544530C1 (de) | 1997-08-28 |
| DE59602327D1 (de) | 1999-08-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3884288T2 (de) | Verfahren und Vorrichtung zum Auftragen eines elastischen Streifens auf ein fortlaufendes Gewebe. | |
| DE2440280C2 (de) | Verfahren zum kontinuierlichen Überziehen mit einer Überzugslösung einer laufenden Bahn | |
| DE8306466U1 (de) | Wegwerfwindel | |
| DE2507116A1 (de) | Vorrichtung zum aufbringen eines beschichtungsmaterials und verfahren unter verwendung derselben | |
| EP0401679B1 (de) | Verfahren und Vorrichtung zum elektrostatischen Aufsprühen einer Flüssigkeitsschicht auf ein Substrat und zum Trocknen der Flüssigkeitsschicht auf dem Substrat | |
| DE2142345C2 (de) | Verfahren zur Herstellung einer Windel u. dgl. | |
| DE8901172U1 (de) | Vorrichtung zum Auftragen eines Klebestoffes auf elastische Fäden | |
| DE2612373A1 (de) | Leiste mit metallueberzug und verfahren zu ihrer herstellung | |
| AT402496B (de) | Verfahren zur herstellung von füllkörpern für verpackungszwecke | |
| DE4032719A1 (de) | Einrichtung zum auftragen von produkten, wie farben oder lacke, mit hilfe von spritzpistolen auf unregelmaessig geformte teile | |
| DE3603749C2 (de) | Zigarettenherstellungsmaschine | |
| DE69109670T2 (de) | Verfahren zur beidseitigen beschichtung einer beweglichen bahn. | |
| EP0967317B1 (de) | Verfahren zum Kantenleimen und Spannaggregat mit einer Vorrichtung zum Kantenleimen | |
| DE2726944A1 (de) | Verfahren und vorrichtung zur herstellung eines aus stehenden fasern bestehenden bahnfoermigen materials | |
| DE69905762T2 (de) | Vorrichtung zum aufbringen eines reflektierenden materials auf ein substrat | |
| DE2949902C2 (da) | ||
| DE2747265A1 (de) | Vorrichtung zum abziehen einer auf einem plattenartigen traeger haftenden folie | |
| DE19544530C1 (de) | Vorrichtung zum elektrostatischen Pulverbeschichten der Vorderseite eines Bandes | |
| DE1596988B2 (de) | Kontinuierliches verfahren zum gleichzeitigen ueberziehen von glastafeln unterschiedlicher groesse bei der spiegelherstellung und vorrichtung zu seiner durchfuehrung | |
| DE1577944A1 (de) | Verfahren und Vorrichtung zum elektrostatischen Beflocken von faden-oder garnfoermigem Material | |
| DE3233061C2 (de) | Vorrichtung zum Bedrucken flexibler Flächenteile | |
| EP0609484B1 (de) | Vorrichtung zum Auftragen von Streichfarbe auf eine Faserstoffbahn | |
| DE1190368B (de) | Vorrichtung zum elektrostatischen Fluessigkeitsauftragen auf im wesentlichen ebene Werkstueckflaechen | |
| EP0793536A1 (de) | Vorrichtung zur farbbeschichtung | |
| DE629418C (de) | Abstaubvorrichtung |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19970326 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT CH DE DK FI FR GB IT LI SE |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 19980929 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT CH DE DK FI FR GB IT LI SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19990630 |
|
| REF | Corresponds to: |
Ref document number: 181681 Country of ref document: AT Date of ref document: 19990715 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: ISLER & PEDRAZZINI AG Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 59602327 Country of ref document: DE Date of ref document: 19990805 |
|
| ET | Fr: translation filed | ||
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19990901 |
|
| ITF | It: translation for a ep patent filed | ||
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20011005 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20011010 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20011011 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DK Payment date: 20011012 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20011017 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20011025 Year of fee payment: 6 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20011029 Year of fee payment: 6 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021018 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021018 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021019 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021031 Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021031 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030501 |
|
| EUG | Se: european patent has lapsed | ||
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20021018 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030630 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20051018 |