EP0816525A1 - Siebplatte - Google Patents
Siebplatte Download PDFInfo
- Publication number
- EP0816525A1 EP0816525A1 EP97109259A EP97109259A EP0816525A1 EP 0816525 A1 EP0816525 A1 EP 0816525A1 EP 97109259 A EP97109259 A EP 97109259A EP 97109259 A EP97109259 A EP 97109259A EP 0816525 A1 EP0816525 A1 EP 0816525A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- sieve plate
- support layer
- plate according
- wear protection
- hard alloy
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
- 239000010410 layer Substances 0.000 claims abstract description 27
- 239000002347 wear-protection layer Substances 0.000 claims abstract description 19
- 229910045601 alloy Inorganic materials 0.000 claims abstract description 16
- 239000000956 alloy Substances 0.000 claims abstract description 16
- 239000000463 material Substances 0.000 claims abstract description 16
- 239000000203 mixture Substances 0.000 claims abstract description 8
- GUTLYIVDDKVIGB-UHFFFAOYSA-N cobalt atom Chemical compound [Co] GUTLYIVDDKVIGB-UHFFFAOYSA-N 0.000 claims abstract description 7
- 239000007787 solid Substances 0.000 claims abstract description 7
- 239000010941 cobalt Substances 0.000 claims abstract description 6
- 229910017052 cobalt Inorganic materials 0.000 claims abstract description 6
- 239000011159 matrix material Substances 0.000 claims abstract description 6
- 229910052804 chromium Inorganic materials 0.000 claims abstract description 5
- 229910052721 tungsten Inorganic materials 0.000 claims abstract description 5
- 229910052796 boron Inorganic materials 0.000 claims abstract description 4
- 229910052799 carbon Inorganic materials 0.000 claims abstract description 4
- 229910052710 silicon Inorganic materials 0.000 claims abstract description 4
- CWYNVVGOOAEACU-UHFFFAOYSA-N Fe2+ Chemical compound [Fe+2] CWYNVVGOOAEACU-UHFFFAOYSA-N 0.000 claims abstract description 3
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 claims description 14
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 claims description 12
- 238000005520 cutting process Methods 0.000 claims description 8
- 229910052742 iron Inorganic materials 0.000 claims description 7
- 239000000843 powder Substances 0.000 claims description 7
- 239000002131 composite material Substances 0.000 claims description 6
- 229910052759 nickel Inorganic materials 0.000 claims description 6
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 claims description 4
- 239000011651 chromium Substances 0.000 claims description 4
- 238000002844 melting Methods 0.000 claims description 4
- 230000008018 melting Effects 0.000 claims description 4
- 238000007873 sieving Methods 0.000 claims description 4
- 239000010937 tungsten Substances 0.000 claims description 4
- ZOXJGFHDIHLPTG-UHFFFAOYSA-N Boron Chemical compound [B] ZOXJGFHDIHLPTG-UHFFFAOYSA-N 0.000 claims description 3
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 claims description 3
- 239000010703 silicon Substances 0.000 claims description 3
- WFKWXMTUELFFGS-UHFFFAOYSA-N tungsten Chemical compound [W] WFKWXMTUELFFGS-UHFFFAOYSA-N 0.000 claims description 3
- 238000007751 thermal spraying Methods 0.000 claims description 2
- 238000010891 electric arc Methods 0.000 claims 1
- 238000012216 screening Methods 0.000 abstract description 3
- 238000004519 manufacturing process Methods 0.000 description 5
- 150000001247 metal acetylides Chemical class 0.000 description 5
- OAICVXFJPJFONN-UHFFFAOYSA-N Phosphorus Chemical compound [P] OAICVXFJPJFONN-UHFFFAOYSA-N 0.000 description 2
- 238000005260 corrosion Methods 0.000 description 2
- 230000007797 corrosion Effects 0.000 description 2
- 229910052751 metal Inorganic materials 0.000 description 2
- 239000002184 metal Substances 0.000 description 2
- 229910052698 phosphorus Inorganic materials 0.000 description 2
- 239000011574 phosphorus Substances 0.000 description 2
- 238000012545 processing Methods 0.000 description 2
- 238000000926 separation method Methods 0.000 description 2
- -1 tungsten carbides Chemical class 0.000 description 2
- 229910001141 Ductile iron Inorganic materials 0.000 description 1
- ZOKXTWBITQBERF-UHFFFAOYSA-N Molybdenum Chemical compound [Mo] ZOKXTWBITQBERF-UHFFFAOYSA-N 0.000 description 1
- 229910000990 Ni alloy Inorganic materials 0.000 description 1
- 229910000831 Steel Inorganic materials 0.000 description 1
- 238000005266 casting Methods 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 238000000576 coating method Methods 0.000 description 1
- 230000008021 deposition Effects 0.000 description 1
- 238000013461 design Methods 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- QFXZANXYUCUTQH-UHFFFAOYSA-N ethynol Chemical group OC#C QFXZANXYUCUTQH-UHFFFAOYSA-N 0.000 description 1
- 230000005496 eutectics Effects 0.000 description 1
- 238000005242 forging Methods 0.000 description 1
- 239000008187 granular material Substances 0.000 description 1
- 238000003698 laser cutting Methods 0.000 description 1
- 238000010309 melting process Methods 0.000 description 1
- 229910052752 metalloid Inorganic materials 0.000 description 1
- 150000002738 metalloids Chemical class 0.000 description 1
- 238000005272 metallurgy Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 229910052750 molybdenum Inorganic materials 0.000 description 1
- 239000011733 molybdenum Substances 0.000 description 1
- 239000002245 particle Substances 0.000 description 1
- 239000008188 pellet Substances 0.000 description 1
- 238000007750 plasma spraying Methods 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
- 238000012549 training Methods 0.000 description 1
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 1
- 238000003466 welding Methods 0.000 description 1
- 238000009736 wetting Methods 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B07—SEPARATING SOLIDS FROM SOLIDS; SORTING
- B07B—SEPARATING SOLIDS FROM SOLIDS BY SIEVING, SCREENING, SIFTING OR BY USING GAS CURRENTS; SEPARATING BY OTHER DRY METHODS APPLICABLE TO BULK MATERIAL, e.g. LOOSE ARTICLES FIT TO BE HANDLED LIKE BULK MATERIAL
- B07B1/00—Sieving, screening, sifting, or sorting solid materials using networks, gratings, grids, or the like
- B07B1/46—Constructional details of screens in general; Cleaning or heating of screens
- B07B1/4609—Constructional details of screens in general; Cleaning or heating of screens constructional details of screening surfaces or meshes
- B07B1/469—Perforated sheet-like material
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C4/00—Coating by spraying the coating material in the molten state, e.g. by flame, plasma or electric discharge
Definitions
- the invention relates to a screen plate Through openings for sieving granular solids.
- the invention has for its object, sieve plates for high to provide abrasive stresses cost-effectively. According to the invention this is achieved in that the screen plate that is in contact with the solids during screening standing side a wear protection layer from a Hard alloy based on nickel or cobalt, which with a support layer made of iron material metallurgically connected is.
- Sieves of this type can e.g. B. for sieving granules or pellets in the field of metallurgy or for stones or Earths can be used.
- Hard materials are particularly carbides, the Carbides of tungsten and chrome are of particular importance.
- Suitable hard alloys contain 0 to 52% by weight of tungsten, 3 up to 30% by weight chromium, 1.0 to 5.0% by weight boron, 1.0 to 5.0% by weight Silicon, 0.05 to 2.0% by weight carbon and the rest nickel and / or cobalt. Alloys of this type have a structure finely divided species-specific hard phase boride and / or carbide in nature. The matrix metal nickel and / or Cobalt forms boron and with the chromium and with the metalloids Silicon together with carbon hard phases, which are in the Microstructure as primary or secondary solidified connections or in Eliminate the form of binary or ternary eutectics. This Hard phases are extremely hard and determine together the properties of the hard alloy with the tough metal matrix with regard to wear resistance and corrosion resistance. The latter is also important because educated Corrosion products the wear resistance of surfaces Reduce.
- the Hard alloy serves as the matrix alloy for the inlaid carbides.
- the proportion of these stored carbides in the wear protection layer is generally 5 to 70% by weight and preferably 25 to 50% by weight if you have a high Wants to achieve wear resistance.
- the hard alloy in addition to the above mentioned components still 3 to 20 wt% iron and / or 2 to Add 10% by weight of phosphorus. Phosphorus increases the viscosity, improves the wetting of the iron material and lowers it the processing temperature of the alloy.
- Other components strong carbide formers such as e.g. B. Be molybdenum.
- the wear protection layer is made with the support layer Iron material metallurgically connected. Generally poses the support layer is made of steel or nodular cast iron. The The thickness of the wear protection layer is usually in Range from 0.5 to 10 mm.
- An expedient development of the invention consists in to form the wear protection layer from a powder mixture, that applied to the support layer and by melting with the support layer is connected.
- the melting takes place usually in an inert atmosphere or in a vacuum Temperatures from 800 to 1200 ° C. This creates one metallurgical bond between the two layers that is no longer separable. Details of hard nickel alloys and the coating of a support layer made of ferrous material are described in DE-A 4 007 734, which deals with the Training of plain bearings deals. There is also that Another possibility described that the powder mixture apply to the support layer by thermal spraying and can then melt.
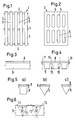
- the sieve plate (1) consists of numerous parallel bars (3) on supporting bars (4) are welded on.
- the ones necessary for screening Through openings are the spaces (5) between the Lattice bars (3).
- the sieve plate (2) of Figure 2 has numerous openings (5) in the form of long looseners on.
- Figure 3 shows in cross section a composite panel with an upper Wear protection layer (8) with the support layer (9) Iron material is connected.
- the bars of the sieve plate (1) in cross section a wedge shape or an approximate wedge shape on, as shown in Figure 5 in three variants. This will expand the passage openings (5) from top to bottom, whereby the jamming of grains completely or largely avoided becomes.
- the passage openings (5) are the Sieve plate (2) according to Figure 2 expanded from top to bottom educated.
- Figure 5 shows, e.g. from a plate-shaped Support layer (9) with applied wear protection layer (8) from, as shown in Figure 3.
- Figure 5 shows, e.g. from a plate-shaped Support layer (9) with applied wear protection layer (8) from, as shown in Figure 3.
- the grooves (10) reduce the thickness of the support layer and facilitate cutting along the lines (11).
- the gutters (10) can e.g. B. also formed when casting the support layer (9) or be formed by forging.
- FIG. 5 (c) In order to produce bars with the profile according to FIG. 5 (c), one proceeds in the representation of FIG Iron material plate made for the support layer (9) is provided and parallel grooves (12) in the surface having.
- the channels (12) with the powder mixture Wear protection layer filled and the connection is through the melting process at temperatures in the range of 800 to 1200 ° C. Possibly after the superficial Grinding the plate with the wear protection there is a separation along the dashed lines (13), so that the wedge profile according to Figure 5 (c) results.
- Of the Parting cut can be from top to bottom or in reverse direction. It can be seen at this production of bars only relatively little material used for the wear protection layer.
- finished Bar profile is the wear protection layer (8) through the softer material of the support layer edged on the sides, taking care that this edge is only very narrow, there it is at least partially removed during operation.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Physics & Mathematics (AREA)
- Plasma & Fusion (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Combined Means For Separation Of Solids (AREA)
- Coating By Spraying Or Casting (AREA)
Abstract
Description
Claims (9)
- Siebplatte mit Durchtrittsöffnungen zum Sieben körniger Feststoffe, dadurch gekennzeichnet, daß die Siebplatte auf der mit den Feststoffen während der Siebung im Kontakt stehenden Seite eine Verschleißschutzschicht aus einer Hartlegierung auf Nickel- oder Kobaltbasis aufweist, die mit einer Stützschicht aus Eisenwerkstoff metallurgisch verbunden ist.
- Siebplatte nach Anspruch 1, dadurch gekennzeichnet, daß die Hartlegierung in ihrer Matrix 5 bis 70 Gew% artfremde Hartstoffe eingebettet enthält.
- Siebplatte nach Anspruch 1 oder 2, dadurch gekennzeichnet, daß die Hartlegierung aus0 bis 52 Gew% Wolfram,3 bis 30 Gew% Chrom,1,0 bis 5,0 Gew% Bor,1,0 bis 5,0 Gew% Silizium,0,05 bis 2,0 Gew% KohlenstoffRest Nickel und/oder Kobalt besteht.
- Siebplatte nach einem der Ansprüche 1 bis 3, dadurch gekennzeichnet, daß die Verschleißschutzschicht aus einem Pulvergemisch gebildet ist, das auf die Stützschicht aufgebracht und durch Schmelzen mit der Stützschicht verbunden ist.
- Siebplatte nach Anspruch 4, dadurch gekennzeichnet, daß das Pulvergemisch durch thermisches Spritzen auf die Stützschicht aufgetragen und eingeschmolzen ist.
- Siebplatte nach Anspruch 4, dadurch gekennzeichnet, daß das Pulvergemisch beim örtlichen Anschmelzen der Stützschicht im Elektrolichtbogen auf die Stützschicht aufgebracht ist.
- Siebplatte nach einem der Ansprüche 1 - 6, dadurch gekennzeichnet, daß die Siebplatte aus mehreren, miteinander verbundenen, etwa parallelen Stäben besteht, wobei jeder Stab eine Verschleißschutzschicht aus der Hartlegierung und eine Stützschicht aus Eisenwerkstoff aufweist, wobei die beiden Schichten metallurgisch miteinander verbunden sind.
- Siebplatte nach Anspruch 7, dadurch gekennzeichnet, daß die Stäbe durch Schneiden aus einer Verbundplatte gebildet sind, wobei die Verbundplatte aus einer Stützschichtplatte besteht, die mit mindestens einer Verschleißschutzschicht versehen ist.
- Siebplatte nach Anspruch 8, dadurch gekennzeichnet, daß die Verbundplatte in den für das Schneiden vorgesehenen Bereichen mit verringerter Dicke der Stützschichtplatte ausgebildet ist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19627039A DE19627039A1 (de) | 1996-07-05 | 1996-07-05 | Siebplatte |
| DE19627039 | 1996-07-05 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| EP0816525A1 true EP0816525A1 (de) | 1998-01-07 |
Family
ID=7798972
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP97109259A Withdrawn EP0816525A1 (de) | 1996-07-05 | 1997-06-07 | Siebplatte |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP0816525A1 (de) |
| DE (1) | DE19627039A1 (de) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2458977A (en) * | 2008-03-31 | 2009-10-07 | Lagan Technology Ltd | Protecting a mesh in asphalt production |
| DE102008042476C5 (de) * | 2008-09-30 | 2018-01-18 | Eipa Eisen Palmen Gmbh | Verfahren zum Herstellen einer Auflage auf einem Träger |
| EP3370887A1 (de) * | 2015-11-06 | 2018-09-12 | Betek GmbH & Co. KG | Werkzeug zum befestigen an einer maschine |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FI124364B (fi) * | 2012-06-15 | 2014-07-15 | Valmet Technologies Inc | Sihtikorin kulutuksenkestävä pinnoite ja menetelmä pinnoitteen valmistamiseksi |
| DE102015213327B4 (de) * | 2015-07-16 | 2020-03-05 | Thyssenkrupp Ag | Siebsegment mit Verschleißschutzelementen |
Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3640760A (en) * | 1970-12-18 | 1972-02-08 | Bird Machine Co | Coated screens |
| US3642519A (en) * | 1969-03-21 | 1972-02-15 | Us Air Force | Method for the development of hard coat seal surfaces |
| DE2651946A1 (de) * | 1975-12-22 | 1977-06-23 | Caterpillar Tractor Co | Verfahren zum aufbringen eines abriebbestaendigen zusammengesetzten ueberzugs auf einen gegenstand |
| JPS60215753A (ja) * | 1984-04-11 | 1985-10-29 | Mitsubishi Heavy Ind Ltd | 溶射・溶融拡散コ−テイング法 |
| DE3437983C1 (de) * | 1984-10-17 | 1986-03-20 | Eisen- und Stahlwerk Pleissner GmbH, 3420 Herzberg | Verfahren zum Aufbringen eines metallischen Schutzüberzuges auf ein metallisches Substrat |
| DE8028806U1 (de) * | 1980-10-29 | 1988-01-28 | Carl Schenck Ag, 6100 Darmstadt | Gegossene Siebplatte |
| DE4007734A1 (de) * | 1990-03-10 | 1991-09-12 | Metallgesellschaft Ag | Gleitlagerung |
-
1996
- 1996-07-05 DE DE19627039A patent/DE19627039A1/de not_active Withdrawn
-
1997
- 1997-06-07 EP EP97109259A patent/EP0816525A1/de not_active Withdrawn
Patent Citations (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3642519A (en) * | 1969-03-21 | 1972-02-15 | Us Air Force | Method for the development of hard coat seal surfaces |
| US3640760A (en) * | 1970-12-18 | 1972-02-08 | Bird Machine Co | Coated screens |
| DE2651946A1 (de) * | 1975-12-22 | 1977-06-23 | Caterpillar Tractor Co | Verfahren zum aufbringen eines abriebbestaendigen zusammengesetzten ueberzugs auf einen gegenstand |
| DE8028806U1 (de) * | 1980-10-29 | 1988-01-28 | Carl Schenck Ag, 6100 Darmstadt | Gegossene Siebplatte |
| JPS60215753A (ja) * | 1984-04-11 | 1985-10-29 | Mitsubishi Heavy Ind Ltd | 溶射・溶融拡散コ−テイング法 |
| DE3437983C1 (de) * | 1984-10-17 | 1986-03-20 | Eisen- und Stahlwerk Pleissner GmbH, 3420 Herzberg | Verfahren zum Aufbringen eines metallischen Schutzüberzuges auf ein metallisches Substrat |
| DE4007734A1 (de) * | 1990-03-10 | 1991-09-12 | Metallgesellschaft Ag | Gleitlagerung |
Non-Patent Citations (1)
| Title |
|---|
| DATABASE WPI Derwent World Patents Index; AN 85-308042 c49, XP002024552, "coating stainless steel to form alloy on surface" * |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2458977A (en) * | 2008-03-31 | 2009-10-07 | Lagan Technology Ltd | Protecting a mesh in asphalt production |
| GB2458977B (en) * | 2008-03-31 | 2012-04-18 | Lagan Technology Ltd | A process and apparatus for producing asphalt |
| DE102008042476C5 (de) * | 2008-09-30 | 2018-01-18 | Eipa Eisen Palmen Gmbh | Verfahren zum Herstellen einer Auflage auf einem Träger |
| EP3370887A1 (de) * | 2015-11-06 | 2018-09-12 | Betek GmbH & Co. KG | Werkzeug zum befestigen an einer maschine |
| EP3370887B1 (de) * | 2015-11-06 | 2025-11-19 | Betek GmbH & Co. KG | Siebvorrichtung zum befestigen an einer siebmaschine |
Also Published As
| Publication number | Publication date |
|---|---|
| DE19627039A1 (de) | 1998-01-08 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE2621472C2 (de) | Verwendung einer Hartlegierung für Schneid-,Scher-oder Verformungswerkzeuge | |
| DE69521292T2 (de) | Verfahren zur herstellung einer schichtwerkstoffen aus metall | |
| EP0145897B1 (de) | Fügeverfahren | |
| DE69802051T2 (de) | Legierungen zum Verbinden auf Sinterkarbid, und damit hergestellte Verbundwerkstoffe | |
| DE2919477C2 (de) | Verschleißfester Verbundwerkstoff, Verfahren zu seiner Herstellung und Verwendung des Verbundwerkstoffes | |
| DE69713806T2 (de) | Aluminium blech und verfahren zum schweissen von bauteilen | |
| DE112009003706T5 (de) | Verbessertes Verfahren und Gegenstand der verschleißfesten Hartauftragsschweißung | |
| DE202015102837U1 (de) | Aufzugsbrems- und/oder Fangvorrichtung mit geschweißtem Bremsbelag | |
| DE19508947A1 (de) | Verschleißfeste, anlaßbeständige und warmfeste Legierung | |
| EP3074166B1 (de) | Verfahren zur herstellung eines vormaterials für ein zerspanungswerkzeug und entsprechendes vormaterial | |
| EP3074167B1 (de) | Verfahren zur herstellung eines vormaterials für ein zerspanungswerkzeug | |
| CH667412A5 (de) | Verfahren zur herstellung einer kokille fuer stahlstranggiessanlagen. | |
| AT411654B (de) | Verfahren zur herstellung eines zerspanungswerkzeuges | |
| AT403668B (de) | Kokille für stranggiessanlagen | |
| DE3437983C1 (de) | Verfahren zum Aufbringen eines metallischen Schutzüberzuges auf ein metallisches Substrat | |
| DE3221884C2 (de) | Verschleißbeständiges Bauteil zur Verwendung in Brennkraftmaschinen | |
| DE19627039A1 (de) | Siebplatte | |
| DE2311400A1 (de) | Lotlegierung | |
| DE3310038C2 (de) | Verfahren zur Herstellung eines Verbundkörpers | |
| WO2025016779A1 (de) | Strangerzeuger zur erzeugung von materialsträngen und verfahren zur herstellung eines derartigen strangerzeugers | |
| DE102013213752B4 (de) | Verfahren zur Herstellung eines Werkzeugs für die Bearbeitung von Blechen sowie Werkzeug | |
| WO2013144043A1 (de) | Werkstück und ein verfahren zur herstellung eines werkstückes | |
| DE102020106476A1 (de) | SCHWEIßEN VON UNGLEICHEN MATERIALIEN MIT MERKMALEN IN DER ANLAGEFLÄCHE | |
| EP2756897A1 (de) | Verfahren zum Herstellen eines als metallischer Verbundwerkstoff ausgeführten Flachprodukts | |
| DE3339118A1 (de) | Verfahren zur herstellung von metallbloecken mit eingelagerten hartstoffkoernern |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): BE DE FR GB NL |
|
| 17P | Request for examination filed |
Effective date: 19980707 |
|
| AKX | Designation fees paid |
Free format text: BE DE FR GB NL |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): BE DE FR GB NL |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: METALLGESELLSCHAFT AKTIENGESELLSCHAFT |
|
| 17Q | First examination report despatched |
Effective date: 20000217 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN WITHDRAWN |
|
| 18W | Application withdrawn |
Withdrawal date: 20000616 |