EP0817687B1 - Verfahren zum herstellen eines bandes aus einem warmgewalzten staab - Google Patents
Verfahren zum herstellen eines bandes aus einem warmgewalzten staab Download PDFInfo
- Publication number
- EP0817687B1 EP0817687B1 EP95915420A EP95915420A EP0817687B1 EP 0817687 B1 EP0817687 B1 EP 0817687B1 EP 95915420 A EP95915420 A EP 95915420A EP 95915420 A EP95915420 A EP 95915420A EP 0817687 B1 EP0817687 B1 EP 0817687B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- rod
- cooling
- process according
- strip
- rolling
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims description 33
- 238000001816 cooling Methods 0.000 claims description 51
- 238000005096 rolling process Methods 0.000 claims description 45
- 239000012809 cooling fluid Substances 0.000 claims description 21
- 238000005507 spraying Methods 0.000 claims description 4
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 4
- 238000005097 cold rolling Methods 0.000 claims description 3
- 238000011144 upstream manufacturing Methods 0.000 claims description 2
- 229910000831 Steel Inorganic materials 0.000 claims 1
- 238000004140 cleaning Methods 0.000 claims 1
- 238000012544 monitoring process Methods 0.000 claims 1
- 239000010959 steel Substances 0.000 claims 1
- 239000007788 liquid Substances 0.000 description 20
- 101100165186 Caenorhabditis elegans bath-34 gene Proteins 0.000 description 13
- 239000002184 metal Substances 0.000 description 11
- 238000004519 manufacturing process Methods 0.000 description 4
- 230000035882 stress Effects 0.000 description 4
- 229910000975 Carbon steel Inorganic materials 0.000 description 3
- 239000010962 carbon steel Substances 0.000 description 3
- RZVAJINKPMORJF-UHFFFAOYSA-N Acetaminophen Chemical compound CC(=O)NC1=CC=C(O)C=C1 RZVAJINKPMORJF-UHFFFAOYSA-N 0.000 description 2
- 101100493705 Caenorhabditis elegans bath-36 gene Proteins 0.000 description 2
- 101100493706 Caenorhabditis elegans bath-38 gene Proteins 0.000 description 2
- 101100493710 Caenorhabditis elegans bath-40 gene Proteins 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 230000003466 anti-cipated effect Effects 0.000 description 1
- 238000009835 boiling Methods 0.000 description 1
- 238000006243 chemical reaction Methods 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 239000002826 coolant Substances 0.000 description 1
- 230000007423 decrease Effects 0.000 description 1
- 230000003247 decreasing effect Effects 0.000 description 1
- 239000007789 gas Substances 0.000 description 1
- 230000008642 heat stress Effects 0.000 description 1
- 238000005098 hot rolling Methods 0.000 description 1
- 239000000203 mixture Substances 0.000 description 1
- 230000003647 oxidation Effects 0.000 description 1
- 238000007254 oxidation reaction Methods 0.000 description 1
- 238000002360 preparation method Methods 0.000 description 1
- 230000003134 recirculating effect Effects 0.000 description 1
- 230000008646 thermal stress Effects 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B1/00—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations
- B21B1/16—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling wire rods, bars, merchant bars, rounds wire or material of like small cross-section
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B37/00—Control devices or methods specially adapted for metal-rolling mills or the work produced thereby
- B21B37/48—Tension control; Compression control
- B21B37/50—Tension control; Compression control by looper control
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B1/00—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations
- B21B1/16—Metal-rolling methods or mills for making semi-finished products of solid or profiled cross-section; Sequence of operations in milling trains; Layout of rolling-mill plant, e.g. grouping of stands; Succession of passes or of sectional pass alternations for rolling wire rods, bars, merchant bars, rounds wire or material of like small cross-section
- B21B1/166—Rolling wire into sections or flat ribbons
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B21—MECHANICAL METAL-WORKING WITHOUT ESSENTIALLY REMOVING MATERIAL; PUNCHING METAL
- B21B—ROLLING OF METAL
- B21B45/00—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills
- B21B45/02—Devices for surface or other treatment of work, specially combined with or arranged in, or specially adapted for use in connection with, metal-rolling mills for lubricating, cooling, or cleaning
- B21B45/0203—Cooling
- B21B45/0209—Cooling devices, e.g. using gaseous coolants
- B21B45/0215—Cooling devices, e.g. using gaseous coolants using liquid coolants, e.g. for sections, for tubes
- B21B45/023—Cooling devices, e.g. using gaseous coolants using liquid coolants, e.g. for sections, for tubes by immersion in a bath
Definitions
- the present invention relates to a process for producing a rectangular strip from a hot rolled, round rod by passing the rod consecutively through a series of rolling mills. More specifically, the invention relates to a process which employs inter-cooling between consecutive rolling mills as well as strip tension control to produce a strip which exceeds currently achievable maximum width to thickness ratios.
- Pinned tubes are employed in many commercial applications as a means to allow heat exchange to occur between mediums of different temperatures without necessitating commingling of the mediums.
- One common design for finned tubes employs a fin constructed of a continuous strip of metal fin material. In cross section, this strip is rectangular in dimension, having a width exceeding its thickness.
- the strip is helically wound around the exterior surface of a hollow tube and secured thereto so that one of the shorter sides of the cross-sectional rectangular shaped strip is secured adjacent to the tube's exterior surface and the width of the strip extends outward away from and perpendicular to the tube's exterior surface.
- one common strip size has a width of 2.032 centimeters (0.80 inches) and a thickness of 0.1938 centimeters (0.047 inches) resulting in a width to thickness ratio of approximately 17.2 to 1.
- the current method for producing strips of the desired dimensions is to begin with a sheet of continuous cold rolled metal, often carbon steel, of the desired thickness.
- the sheet is then slit into strips of the desired width. This is briefly described in an article entitled "The Rolling of Round Wire into Flats/Rectangles" published in the October, 1959 issue of FENN Engineering News , a publication by Fenn Manufacturing Co., Newington, Connecticut, U.S.A.
- the sheets are uniformly rolled to close tolerances. The price of these sheets reflects the time and effort required to roll them to close tolerances. When the cost of sitting the sheets is added to the cost of the sheets, the total cost to produce strips according to current methods is quite expensive.
- current methods for converting a rod into a strip are limited to creation of strips with width to thickness ratios of less than approximately 12 to 1.
- current methods are employed to create strips having width to thickness ratios exceeding approximately 12 to 1, for example having ratios of 15 to 1 or 17 to 1, during the rolling process the metal strip develops severe edge fractures. These fractures cause the strip to break. The cause these fractures appear to be two-fold.
- heat is added to the metal until the metal finally reaches a temperature at which it fails, causing it to fracture or break.
- Second, in addition to the heat stress exerted on the metal mechanical stress is inflicted on the metal by the tug on the rod from the subsequent rolling mill as it pulls the rod toward the mill.
- the present invention addresses this problem of limited width to thickness ratio by providing a method for producing strips from rods which utilizes cooling and tension controls between adjacent rolling mills in order to minimize tension on the material being rolled so that it is possible to produce strips having width to thickness ratios of up to approximately 17 to 1.
- the present invention is a cold rolling processes, and as such, should be distinguished from hot rolling processes such as those described in EP-A O 314 667.
- the present invention is a process for creating strips from hot rolled metal rods such that the strip which is produced achieves a width to thickness ratio of approximately 17 to 1.
- the process consists of cooling the rod after it passes through each consecutive rolling mill to reduce the thermal stress on the rod and employs tension controllers following each consecutive rolling mill in order to control the previous rolling mill and thereby reduce the mechanical stress on the rod. Cooling is preferably accomplished by immersing the rod in a liquid cooling bath and/or by spraying cooling fluid directly on the rod.
- FIG. 1 there is diagrammatically illustrated a process according to a preferred embodiment of the present invention for converting a rod 10 , such as a hot rolled rod of carbon steel, into a strip 12 suitable for use as a fin for a finned tube (not illustrated) or for other commercial applications.
- a rod 10 such as a hot rolled rod of carbon steel
- a strip 12 suitable for use as a fin for a finned tube (not illustrated) or for other commercial applications.
- a spool 14 of rolled up rod 10 which is next unwound through an eye 16 .
- the purpose of the eye 16 is to prevent the rod 10 from becoming tangled or kinked as it unwinds from the spool 14 .
- the rod 10 enters a descaler 18 which removes any scale or oxidation product present on the surface of the rod 10 .
- the rod 10 enters a straightener 20 which straightens the rod 10 in preparation for entering a rolling train portion 22 of the process.
- the rolling train portion 22 consists of a plurality of rolling mills 24 , 26 , 28 , 30 , etc. arranged in series, with each individual rolling mill 24 , 26 , 28 , or 30 , being followed by its respective liquid cooling bath 34 , 36 , 38 or 40 .
- the strip 12 has a width 42 and a thickness 44 measured perpendicular to its width 42 .
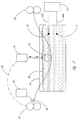
- FIG 7 there is shown in enlarged detail a preferred arrangement of the first liquid cooling bath 34 .
- the first liquid cooling bath 34 is filled with a cooling fluid 46 , such as water, which enters the first liquid cooling bath 34 via an inlet 48 and exits the first liquid cooling bath 34 via an outlet 50 as will be further explained hereafter.
- the rod 10 exits from the first rolling mill 24 upstream of the first liquid cooling bath 34 .
- the rod 10 then enters the first liquid cooling bath 34 where the rod 10 is cooled by direct contact with the cooling fluid 46 .
- the rod 10 is immersed in the cooling fluid as the rod 10 passes under a roller 52 provided on a tension controller 54 before reemerging from the first liquid cooling bath 34 in order to travel through the second rolling mill 26 .
- the roller 52 is in rolling contact with the rod 10 which passes under the roller 52 as the rod 10 travels through the first liquid cooling bath 34 .
- the roller 52 responds to increases in tension in the rod 10 by moving upwardly and responds to decreases in tension in the rod 10 by moving downwardly.
- This upward and downward movement is illustrated by the arrows shown in Figure 7.
- This upward and downward movement is translated into an electronic signal which controls the drive speed of the preceding first rolling mill 24 , as is illustrated in Figure 7 schematically by a broken line 56 which connects the tension controller 54 and the first rolling mill 24 .
- By controlling the speed of the preceding first rolling mill 24 mechanical stress is decreased on the rod 10 as the rod 10 exits the first rolling mill 24 .
- warm cooling fluid 46-W is continuously removed via the outlet 50 , cooled by passing it through a conventional heat exchange process 57 , and then recirculating cool cooling fluid 46-C back to the first liquid cooling bath 34 via the inlet 48 .
- cooling nozzles 58 are optionally provided at each of the rolling mills 24 , 26 , 28 , and 30 .
- the purpose for these cooling nozzles 58 is to provide additional cooling in the form of cooling fluid 46 which is supplied from a cooling fluid source 60 .
- the cooling fluid 46 enters the cooling nozzles 58 from the cooling fluid source 60 and is emitted from the cooling nozzles 58 , impinging directly on the heated rod 10 as the rod 10 passes through each of the rolling mills 24 , 26 , 28 , and 30 .
- cooling nozzles 58 may be used solely to provide the necessary cooling of the rod 10 , thereby eliminating the need for cooling baths 34-40 .
- cooling nozzles 58 and the cooling baths 34-40 have been described for use with cooling fluid 46 , other coolants, not illustrated, such as liquids or gases may be substituted for the cooling fluid, and other alternate cooling means, not illustrated, may be employed instead of either cooling nozzles 58 or cooling baths 34-40 .
- the strip 12 is rewound into a spool 62 , as illustrated in Figure 1.
- the spool 62 of strip 12 is then ready for use or for further processing.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Metal Rolling (AREA)
- Heat Treatment Of Strip Materials And Filament Materials (AREA)
- Casting Or Compression Moulding Of Plastics Or The Like (AREA)
- Laminated Bodies (AREA)
Claims (13)
- Kaltwalzverfahren zum Erzeugen eines Bandes (12) aus einem Stab bzw. einer Stange (10), umfassend:Leiten bzw. Führen eines Stabs (10) durch eine Reihe von Kaltbearbeitungs-Walzwerken (24-30),Abkühlen des Stabs (10), während der Stab (10) zwischen aufeinanderfolgenden Walzwerken (24-30) hindurchläuft, undMinimieren der Zugspannung im Stab (10), während der Stab (10) zwischen aufeinanderfolgenden Walzwerken (24-30) hindurchläuft.
- Verfahren gemäß Anspruch 1, wobei das Abkühlen des Stabs (10) durch Eintauchen des Stabs (10) in ein Kühlfluid (46) erfolgt.
- Verfahren gemäß Anspruch 2, wobei das Abkühlen des Stabs (10) ferner durch Aufsprühen von Kühlfluid auf den Stab (10) erfolgt.
- Verfahren gemäß Anspruch 1, wobei das Abkühlen des Stabs (10) durch Aufsprühen von Kühlfluid (46) auf den Stab (10) erfolgt.
- Verfahren gemäß einem der vorangehenden Ansprüche, wobei das verwendete Kühlfluid (46) Wasser ist.
- Verfahren gemäß Anspruch 1, ferner umfassend:Überwachen bzw. Steuern der Zugspannung im Stab (10) unmittelbar stromab jedes Walzwerks (24-30) mit einem Zugspannungsregler (54) und Anwenden des Zugspannungsreglers (54) zur Regelung der Geschwindigkeit eines anschließenden, stromaufseitigen Walzwerks (24-28).
- Verfahren gemäß Anspruch 1, ferner umfassend:Reinigen und Geraderichten des Stabs (10) vor dem Leiten bzw. Führen des Stabs (10) durch die Reihe von Kaltbearbeitungs-Walzwerken (24-30).
- Verfahren gemäß einem der Ansprüche 1 und 7, wobei der Stab (10) aus Stahl besteht.
- Verfahren gemäß Anspruch 8, wobei die Abkühlung durch Eintauchen des Stabs (10) in ein mit Kühlfluid (46) gefülltes Kühlbad (34-40) erfolgt.
- Verfahren gemäß Anspruch 9, wobei das Kühlbad (34-40) mit Wasser gefüllt ist bzw. wird.
- Verfahren gemäß Anspruch 10, wobei die Abkühlung ferner durch Aufsprühen von Kühlfluid (46) auf den Stab (10) aus an jedem Walzwerk (24-30) gelegenen Kühlungsdüsen (58) erfolgt.
- Verfahren gemäß Anspruch 11, wobei das Kühlfluid (46) Wasser ist.
- Verfahren gemäß Anspruch 8, wobei die Geschwindigkeit jedes der Walzwerke (24-30) durch einen Zugspannungsregler (54) gesteuert wird, der fortlaufend die Zugspannung des Stabs (10) überwacht.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| AT95915420T ATE180999T1 (de) | 1995-03-31 | 1995-03-31 | Verfahren zum herstellen eines bandes aus einem warmgewalzten staab |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PCT/US1995/003752 WO1996030135A1 (en) | 1995-03-31 | 1995-03-31 | Process for making a strip from a hot rolled rod |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0817687A1 EP0817687A1 (de) | 1998-01-14 |
| EP0817687B1 true EP0817687B1 (de) | 1999-06-09 |
Family
ID=22248877
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP95915420A Expired - Lifetime EP0817687B1 (de) | 1995-03-31 | 1995-03-31 | Verfahren zum herstellen eines bandes aus einem warmgewalzten staab |
Country Status (7)
| Country | Link |
|---|---|
| EP (1) | EP0817687B1 (de) |
| JP (1) | JP2989670B2 (de) |
| KR (1) | KR100232421B1 (de) |
| DE (1) | DE69510236T2 (de) |
| DK (1) | DK0817687T3 (de) |
| ES (1) | ES2135054T3 (de) |
| WO (1) | WO1996030135A1 (de) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| SI4489884T1 (sl) * | 2023-01-18 | 2025-12-31 | Nanoform Finland Oyj | Postopek za kristalizacijo zdravilnih učinkovin |
Family Cites Families (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE81919C (de) * | ||||
| US2226948A (en) | 1936-01-11 | 1940-12-31 | Simons Abraham | Method of rolling |
| FR1283328A (fr) * | 1960-12-23 | 1962-02-02 | Thomson Houston Comp Francaise | Laminage continu à froid à grande vitesse |
| US3466907A (en) * | 1966-01-03 | 1969-09-16 | Lincoln Electric Co | Metal ribbon,welding electrodes and method and apparatus for forming same |
| FR2196207A1 (de) * | 1972-08-18 | 1974-03-15 | Morgan Construction Co | |
| JPS57168716A (en) * | 1981-04-10 | 1982-10-18 | Mitsubishi Heavy Ind Ltd | Tension controlling method of rolling material |
| AT393361B (de) | 1987-10-29 | 1991-10-10 | Boehler Gmbh | Verfahren und Vorrichtung zur Erzeugung dünner Drähte, Stäbe, Rohre und Profile aus Stählen und Legierungen mit geringem Formänderungsverm¦gen, insbes. aus härtbaren Stählen. |
| AT394670B (de) * | 1990-02-13 | 1992-05-25 | Boehler Gmbh | Verfahren und anordnung zum walzen von drahtund stabmaterial |
-
1995
- 1995-03-31 EP EP95915420A patent/EP0817687B1/de not_active Expired - Lifetime
- 1995-03-31 DE DE69510236T patent/DE69510236T2/de not_active Expired - Fee Related
- 1995-03-31 WO PCT/US1995/003752 patent/WO1996030135A1/en not_active Ceased
- 1995-03-31 KR KR1019970706865A patent/KR100232421B1/ko not_active Expired - Fee Related
- 1995-03-31 ES ES95915420T patent/ES2135054T3/es not_active Expired - Lifetime
- 1995-03-31 DK DK95915420T patent/DK0817687T3/da active
- 1995-03-31 JP JP52929296A patent/JP2989670B2/ja not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| DE69510236D1 (de) | 1999-07-15 |
| KR100232421B1 (ko) | 1999-12-01 |
| WO1996030135A1 (en) | 1996-10-03 |
| DE69510236T2 (de) | 1999-11-04 |
| ES2135054T3 (es) | 1999-10-16 |
| DK0817687T3 (da) | 1999-11-15 |
| JPH10512198A (ja) | 1998-11-24 |
| JP2989670B2 (ja) | 1999-12-13 |
| KR19980703461A (ko) | 1998-11-05 |
| EP0817687A1 (de) | 1998-01-14 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US5329688A (en) | Process and plant for obtaining steel strip coils having cold-rolled characteristics and directly obtained in a hot-rolling line | |
| KR950014488B1 (ko) | 연속 주조 방법에 따라 강제품을 연속으로 제조하는 방법 및 장치 | |
| LT3832B (en) | Method for obtaining of steel tape by hot rolling, tape device for pouring out | |
| EP0611610A1 (de) | Verfahren zum Herstellen eines Bandes, Vorstreifens oder einer Bramme | |
| SU1569050A1 (ru) | Способ изготовлени гнутых профилей | |
| EP0761326A1 (de) | Warmbandproduktionsanlage für das Walzen von dünnem Walzband | |
| DE69909332T2 (de) | Integriertes kontinuierliches stranggiess- und inline warmwalzverfahren sowie entsprechendes verfahren mit zwischenwickeln und abwickeln des vorstreifens | |
| KR960033577A (ko) | 열간압연방법 및 장치 | |
| US6763561B2 (en) | Continuous casting and hot rolling apparatus for parallel production of multiple metal shapes | |
| JPH08294715A (ja) | ストリップ連続鋳造熱間圧延熱処理設備およびストリップ連続鋳造熱間圧延熱処理方法 | |
| US5437089A (en) | Method and apparatus for continuous production hot-rolled strips | |
| US5638714A (en) | Process for making a strip from a rod | |
| JPS62187505A (ja) | 熱間鋼帯の製造方法および設備 | |
| DE4243857C1 (de) | Verfahren zum Herstellen eines Stahlbandes durch Gießen eines Stranges und anschließendes Walzen | |
| AT404907B (de) | Verfahren und anlage zum herstellen von edelstahlband | |
| EP0817687A1 (de) | Verfahren zum herstellen eines bandes aus einem warmgewalzten staab | |
| CA1070990A (en) | Method and apparatus for hot rolling a thin metal sheet | |
| EP2543449A1 (de) | Verfahren zur Herstellung von Magnesiumband | |
| MXPA97007289A (en) | Process to produce a strip of a laminated rod calie | |
| US4936132A (en) | Continuous hot rolling process for making thin steel strip | |
| JPH11207403A (ja) | 熱間鋼板圧延設備及び圧延方法 | |
| RU2146974C1 (ru) | Способ производства бесконечной горячекатаной полосы на непрерывно-реверсивном литейно-прокатном агрегате | |
| EP1539389B1 (de) | Verfahren zum erzielen von mindestens zwei separat aufgewickelten einzelsträngen von zeitgleich stranggepressten einzelrohren unter verwendung einer spuleinrichtung | |
| RU2044580C1 (ru) | Способ производства горячекатаных полос | |
| DE2414475C3 (de) | Verfahren zum Walzen von zu haspelndem starkem Walzband und zur Durchführung dieses Verfahrens verwendete Anstellvorrichtung für Walzgerüste |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19970818 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE DE DK ES FR GB IT NL |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 19980928 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE DE DK ES FR GB IT NL |
|
| REF | Corresponds to: |
Ref document number: 180999 Country of ref document: AT Date of ref document: 19990615 Kind code of ref document: T |
|
| REF | Corresponds to: |
Ref document number: 69510236 Country of ref document: DE Date of ref document: 19990715 |
|
| ITF | It: translation for a ep patent filed | ||
| ET | Fr: translation filed | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2135054 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: TP |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E |
|
| NLS | Nl: assignments of ep-patents |
Owner name: FINTUBE TECHNOLOGIES, INC. |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: PC2A |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20010228 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20010313 Year of fee payment: 7 Ref country code: DK Payment date: 20010313 Year of fee payment: 7 Ref country code: AT Payment date: 20010313 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20010326 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20010328 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20010330 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20010515 Year of fee payment: 7 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020331 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020331 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020401 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20020402 |
|
| BERE | Be: lapsed |
Owner name: *FINTUBE TECHNOLOGIES INC. Effective date: 20020331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021001 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021001 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20020331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20021129 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 20021001 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20030410 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050331 |