EP0848079B1 - Verfahren zur Herstellung einer Schutzbeschichtung mit grosser Wirksamkeit gegen Hochtemperatur-Verschleiss von Superlegierungen, Schutzbeschichtung und damit beschichtete Teile - Google Patents
Verfahren zur Herstellung einer Schutzbeschichtung mit grosser Wirksamkeit gegen Hochtemperatur-Verschleiss von Superlegierungen, Schutzbeschichtung und damit beschichtete Teile Download PDFInfo
- Publication number
- EP0848079B1 EP0848079B1 EP97402999A EP97402999A EP0848079B1 EP 0848079 B1 EP0848079 B1 EP 0848079B1 EP 97402999 A EP97402999 A EP 97402999A EP 97402999 A EP97402999 A EP 97402999A EP 0848079 B1 EP0848079 B1 EP 0848079B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- coating
- deposit
- powder
- process according
- protective coating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000576 coating method Methods 0.000 title claims description 96
- 239000011248 coating agent Substances 0.000 title claims description 72
- 238000000034 method Methods 0.000 title claims description 50
- 229910000601 superalloy Inorganic materials 0.000 title claims description 28
- 238000005260 corrosion Methods 0.000 title claims description 16
- 230000007797 corrosion Effects 0.000 title claims description 16
- 239000011253 protective coating Substances 0.000 title claims description 16
- 238000000151 deposition Methods 0.000 title description 17
- BASFCYQUMIYNBI-UHFFFAOYSA-N platinum Chemical group [Pt] BASFCYQUMIYNBI-UHFFFAOYSA-N 0.000 claims description 69
- 239000000843 powder Substances 0.000 claims description 51
- 229910045601 alloy Inorganic materials 0.000 claims description 34
- 239000000956 alloy Substances 0.000 claims description 34
- 229910052697 platinum Inorganic materials 0.000 claims description 30
- 229910052751 metal Inorganic materials 0.000 claims description 27
- 239000002184 metal Substances 0.000 claims description 27
- 230000008569 process Effects 0.000 claims description 24
- 229910052782 aluminium Inorganic materials 0.000 claims description 19
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims description 17
- 239000011651 chromium Substances 0.000 claims description 17
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 claims description 15
- 229910052804 chromium Inorganic materials 0.000 claims description 15
- 230000003647 oxidation Effects 0.000 claims description 14
- 238000007254 oxidation reaction Methods 0.000 claims description 14
- 230000008021 deposition Effects 0.000 claims description 13
- 229910052727 yttrium Inorganic materials 0.000 claims description 11
- VWQVUPCCIRVNHF-UHFFFAOYSA-N yttrium atom Chemical compound [Y] VWQVUPCCIRVNHF-UHFFFAOYSA-N 0.000 claims description 11
- KDLHZDBZIXYQEI-UHFFFAOYSA-N Palladium Chemical compound [Pd] KDLHZDBZIXYQEI-UHFFFAOYSA-N 0.000 claims description 10
- 238000011049 filling Methods 0.000 claims description 6
- 238000010438 heat treatment Methods 0.000 claims description 6
- 150000002739 metals Chemical class 0.000 claims description 6
- 239000004411 aluminium Substances 0.000 claims description 5
- 229910052763 palladium Inorganic materials 0.000 claims description 5
- 239000011230 binding agent Substances 0.000 claims description 3
- 238000010422 painting Methods 0.000 claims description 3
- KJTLSVCANCCWHF-UHFFFAOYSA-N Ruthenium Chemical compound [Ru] KJTLSVCANCCWHF-UHFFFAOYSA-N 0.000 claims description 2
- 230000004888 barrier function Effects 0.000 claims description 2
- 229910052741 iridium Inorganic materials 0.000 claims description 2
- GKOZUEZYRPOHIO-UHFFFAOYSA-N iridium atom Chemical compound [Ir] GKOZUEZYRPOHIO-UHFFFAOYSA-N 0.000 claims description 2
- 229910052747 lanthanoid Inorganic materials 0.000 claims description 2
- 150000002602 lanthanoids Chemical class 0.000 claims description 2
- 229910052762 osmium Inorganic materials 0.000 claims description 2
- SYQBFIAQOQZEGI-UHFFFAOYSA-N osmium atom Chemical compound [Os] SYQBFIAQOQZEGI-UHFFFAOYSA-N 0.000 claims description 2
- 229910052703 rhodium Inorganic materials 0.000 claims description 2
- 239000010948 rhodium Substances 0.000 claims description 2
- MHOVAHRLVXNVSD-UHFFFAOYSA-N rhodium atom Chemical compound [Rh] MHOVAHRLVXNVSD-UHFFFAOYSA-N 0.000 claims description 2
- 229910052707 ruthenium Inorganic materials 0.000 claims description 2
- 239000000203 mixture Substances 0.000 description 15
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 description 11
- PNEYBMLMFCGWSK-UHFFFAOYSA-N aluminium oxide Inorganic materials [O-2].[O-2].[O-2].[Al+3].[Al+3] PNEYBMLMFCGWSK-UHFFFAOYSA-N 0.000 description 9
- 238000000137 annealing Methods 0.000 description 9
- 238000004519 manufacturing process Methods 0.000 description 9
- 229910000951 Aluminide Inorganic materials 0.000 description 8
- 239000000243 solution Substances 0.000 description 8
- 239000010410 layer Substances 0.000 description 7
- 239000002245 particle Substances 0.000 description 7
- 239000010970 precious metal Substances 0.000 description 7
- 239000000758 substrate Substances 0.000 description 6
- 239000012808 vapor phase Substances 0.000 description 6
- 229910000943 NiAl Inorganic materials 0.000 description 5
- 238000011161 development Methods 0.000 description 5
- 238000009792 diffusion process Methods 0.000 description 5
- 239000003607 modifier Substances 0.000 description 5
- 229910052759 nickel Inorganic materials 0.000 description 5
- 239000012071 phase Substances 0.000 description 5
- 150000003839 salts Chemical class 0.000 description 5
- 238000007751 thermal spraying Methods 0.000 description 5
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 description 4
- NPXOKRUENSOPAO-UHFFFAOYSA-N Raney nickel Chemical compound [Al].[Ni] NPXOKRUENSOPAO-UHFFFAOYSA-N 0.000 description 4
- 238000005269 aluminizing Methods 0.000 description 4
- 238000009826 distribution Methods 0.000 description 4
- 239000000446 fuel Substances 0.000 description 4
- 229910001092 metal group alloy Inorganic materials 0.000 description 4
- 229910052684 Cerium Inorganic materials 0.000 description 3
- 229910001252 Pd alloy Inorganic materials 0.000 description 3
- 230000001464 adherent effect Effects 0.000 description 3
- 230000008901 benefit Effects 0.000 description 3
- 229910017052 cobalt Inorganic materials 0.000 description 3
- 239000010941 cobalt Substances 0.000 description 3
- GUTLYIVDDKVIGB-UHFFFAOYSA-N cobalt atom Chemical compound [Co] GUTLYIVDDKVIGB-UHFFFAOYSA-N 0.000 description 3
- 238000001962 electrophoresis Methods 0.000 description 3
- 238000009713 electroplating Methods 0.000 description 3
- 229910052735 hafnium Inorganic materials 0.000 description 3
- 239000000463 material Substances 0.000 description 3
- 239000003973 paint Substances 0.000 description 3
- 230000001681 protective effect Effects 0.000 description 3
- 150000003467 sulfuric acid derivatives Chemical class 0.000 description 3
- 229910052726 zirconium Inorganic materials 0.000 description 3
- XKRFYHLGVUSROY-UHFFFAOYSA-N Argon Chemical compound [Ar] XKRFYHLGVUSROY-UHFFFAOYSA-N 0.000 description 2
- 229910000990 Ni alloy Inorganic materials 0.000 description 2
- QVGXLLKOCUKJST-UHFFFAOYSA-N atomic oxygen Chemical compound [O] QVGXLLKOCUKJST-UHFFFAOYSA-N 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 2
- 239000004568 cement Substances 0.000 description 2
- 238000002485 combustion reaction Methods 0.000 description 2
- 238000007796 conventional method Methods 0.000 description 2
- 230000000694 effects Effects 0.000 description 2
- 238000001652 electrophoretic deposition Methods 0.000 description 2
- 238000005516 engineering process Methods 0.000 description 2
- 230000008020 evaporation Effects 0.000 description 2
- 238000001704 evaporation Methods 0.000 description 2
- 238000004880 explosion Methods 0.000 description 2
- 230000003993 interaction Effects 0.000 description 2
- 229910052746 lanthanum Inorganic materials 0.000 description 2
- 239000013528 metallic particle Substances 0.000 description 2
- 229910000907 nickel aluminide Inorganic materials 0.000 description 2
- 239000001301 oxygen Substances 0.000 description 2
- 229910052760 oxygen Inorganic materials 0.000 description 2
- 238000012545 processing Methods 0.000 description 2
- 239000011241 protective layer Substances 0.000 description 2
- 230000001012 protector Effects 0.000 description 2
- 239000006104 solid solution Substances 0.000 description 2
- 238000004381 surface treatment Methods 0.000 description 2
- 239000000725 suspension Substances 0.000 description 2
- 238000005382 thermal cycling Methods 0.000 description 2
- LSGOVYNHVSXFFJ-UHFFFAOYSA-N vanadate(3-) Chemical class [O-][V]([O-])([O-])=O LSGOVYNHVSXFFJ-UHFFFAOYSA-N 0.000 description 2
- UGFAIRIUMAVXCW-UHFFFAOYSA-N Carbon monoxide Chemical compound [O+]#[C-] UGFAIRIUMAVXCW-UHFFFAOYSA-N 0.000 description 1
- MYMOFIZGZYHOMD-UHFFFAOYSA-N Dioxygen Chemical compound O=O MYMOFIZGZYHOMD-UHFFFAOYSA-N 0.000 description 1
- 229910001029 Hf alloy Inorganic materials 0.000 description 1
- UFHFLCQGNIYNRP-UHFFFAOYSA-N Hydrogen Chemical compound [H][H] UFHFLCQGNIYNRP-UHFFFAOYSA-N 0.000 description 1
- 229910017855 NH 4 F Inorganic materials 0.000 description 1
- 229910000629 Rh alloy Inorganic materials 0.000 description 1
- NINIDFKCEFEMDL-UHFFFAOYSA-N Sulfur Chemical compound [S] NINIDFKCEFEMDL-UHFFFAOYSA-N 0.000 description 1
- QCWXUUIWCKQGHC-UHFFFAOYSA-N Zirconium Chemical compound [Zr] QCWXUUIWCKQGHC-UHFFFAOYSA-N 0.000 description 1
- 239000012190 activator Substances 0.000 description 1
- 238000005054 agglomeration Methods 0.000 description 1
- 230000002776 aggregation Effects 0.000 description 1
- 238000013019 agitation Methods 0.000 description 1
- 229910052786 argon Inorganic materials 0.000 description 1
- 230000000712 assembly Effects 0.000 description 1
- 238000000429 assembly Methods 0.000 description 1
- 238000000889 atomisation Methods 0.000 description 1
- 239000010953 base metal Substances 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 238000005266 casting Methods 0.000 description 1
- 150000001768 cations Chemical class 0.000 description 1
- GWXLDORMOJMVQZ-UHFFFAOYSA-N cerium Chemical compound [Ce] GWXLDORMOJMVQZ-UHFFFAOYSA-N 0.000 description 1
- 238000007596 consolidation process Methods 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 238000004320 controlled atmosphere Methods 0.000 description 1
- 125000004122 cyclic group Chemical group 0.000 description 1
- 230000003247 decreasing effect Effects 0.000 description 1
- 238000000280 densification Methods 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 238000005474 detonation Methods 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 238000004090 dissolution Methods 0.000 description 1
- 230000005684 electric field Effects 0.000 description 1
- 238000005868 electrolysis reaction Methods 0.000 description 1
- 238000004453 electron probe microanalysis Methods 0.000 description 1
- 230000007613 environmental effect Effects 0.000 description 1
- 239000003344 environmental pollutant Substances 0.000 description 1
- 239000003546 flue gas Substances 0.000 description 1
- 239000007789 gas Substances 0.000 description 1
- VBJZVLUMGGDVMO-UHFFFAOYSA-N hafnium atom Chemical compound [Hf] VBJZVLUMGGDVMO-UHFFFAOYSA-N 0.000 description 1
- 239000001257 hydrogen Substances 0.000 description 1
- 229910052739 hydrogen Inorganic materials 0.000 description 1
- 230000003116 impacting effect Effects 0.000 description 1
- 229910052742 iron Inorganic materials 0.000 description 1
- 230000000873 masking effect Effects 0.000 description 1
- 238000005259 measurement Methods 0.000 description 1
- 230000007246 mechanism Effects 0.000 description 1
- 230000005012 migration Effects 0.000 description 1
- 238000013508 migration Methods 0.000 description 1
- 230000007935 neutral effect Effects 0.000 description 1
- 125000002524 organometallic group Chemical group 0.000 description 1
- TWNQGVIAIRXVLR-UHFFFAOYSA-N oxo(oxoalumanyloxy)alumane Chemical compound O=[Al]O[Al]=O TWNQGVIAIRXVLR-UHFFFAOYSA-N 0.000 description 1
- 230000035515 penetration Effects 0.000 description 1
- 230000002688 persistence Effects 0.000 description 1
- 238000005240 physical vapour deposition Methods 0.000 description 1
- 238000007747 plating Methods 0.000 description 1
- 150000003057 platinum Chemical class 0.000 description 1
- PXXKQOPKNFECSZ-UHFFFAOYSA-N platinum rhodium Chemical compound [Rh].[Pt] PXXKQOPKNFECSZ-UHFFFAOYSA-N 0.000 description 1
- 231100000719 pollutant Toxicity 0.000 description 1
- 239000011148 porous material Substances 0.000 description 1
- 238000004663 powder metallurgy Methods 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- 238000004062 sedimentation Methods 0.000 description 1
- 238000007711 solidification Methods 0.000 description 1
- 230000008023 solidification Effects 0.000 description 1
- 238000004544 sputter deposition Methods 0.000 description 1
- 239000000126 substance Substances 0.000 description 1
- 150000004763 sulfides Chemical class 0.000 description 1
- 229910052717 sulfur Inorganic materials 0.000 description 1
- 239000011593 sulfur Substances 0.000 description 1
- 230000003746 surface roughness Effects 0.000 description 1
- 230000007704 transition Effects 0.000 description 1
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C26/00—Coating not provided for in groups C23C2/00 - C23C24/00
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C10/00—Solid state diffusion of only metal elements or silicon into metallic material surfaces
- C23C10/28—Solid state diffusion of only metal elements or silicon into metallic material surfaces using solids, e.g. powders, pastes
- C23C10/34—Embedding in a powder mixture, i.e. pack cementation
- C23C10/58—Embedding in a powder mixture, i.e. pack cementation more than one element being diffused in more than one step
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12771—Transition metal-base component
- Y10T428/12861—Group VIII or IB metal-base component
- Y10T428/12875—Platinum group metal-base component
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12771—Transition metal-base component
- Y10T428/12861—Group VIII or IB metal-base component
- Y10T428/12931—Co-, Fe-, or Ni-base components, alternative to each other
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/12—All metal or with adjacent metals
- Y10T428/12493—Composite; i.e., plural, adjacent, spatially distinct metal components [e.g., layers, joint, etc.]
- Y10T428/12771—Transition metal-base component
- Y10T428/12861—Group VIII or IB metal-base component
- Y10T428/12944—Ni-base component
Definitions
- the invention relates to a method for producing coatings. protectors against high temperature oxidation and hot corrosion of superalloy parts, a coating protector obtained by such a process and parts made of superalloy protected by this coating. Application including the protection of hot parts of superalloy turbomachinery.
- Turbine engine manufacturers both terrestrial that aeronautics, have faced for more than thirty years imperatives to increase the efficiency of turbomachines, reduction in their specific fuel consumption as well as pollutant emissions of COx, SOx, NOx and unburnt.
- One of the ways to meet these imperatives is to get closer to the combustion stoichiometry fuel and therefore increase the gas temperature leaving the combustion chamber and impacting the first turbine stages. It is then necessary to return the turbine materials compatible with this elevation of flue gas temperature.
- One solution is to develop the refractoriness of the materials used to increase the temperature limit for use and service life by creep and fatigue. This solution has been widely implemented work during the appearance of superalloys based on nickel and / or cobalt. It has experienced a technical evolution considerable by the transition from equiaxed superalloys to monocrystalline superalloys (gain of 80 to 100 ° C in creep).
- the coatings belonging to the family of simple aluminides and their derivatives essentially consist of a nickel aluminide alloy NiAl comprising an atomic percentage of aluminum of between 40 and 55%.
- NiAl nickel aluminide alloy
- This type of alloy forms by oxidation at high temperature a protective layer of aluminum oxide limiting the interaction of the coating with the environment (oxygen, molten salts, SO 2 / SO 3 ).
- These coatings can be deposited thermochemically by case hardening or in the vapor phase. They can also be obtained by depositing aluminizing paint followed by appropriate annealing.
- the main advantage of these coatings lies in their simplicity of implementation, low production costs, the possibility of homogeneously coating parts of complex shape.
- a good way to significantly increase lifespan of these coatings is to modify the simple aluminide NiAl by different elements such as chromium and / or certain precious metals from the platinum mine.
- the operation consists then to make a pre-deposit on the superalloy part or modifier metals, followed by aluminization.
- a specific heat treatment is carried out between the so-called pre-deposition step of the modifier metal and the actual aluminization step.
- chromium as a modifier metal is described for example in French patent 2,559,508 filed by SNECMA.
- chromium can be applied by way thermochemical.
- the role of chromium is then essentially limit the acidity or basicity of molten salts by so-called hot corrosion conditions, by dissolution of cations playing the acid-base role of buffer in salt molten.
- platinum as a modifier metal is described in particular by patent FR 2 018 097.
- platinum can be deposited electrolytically on the workpiece superalloy. This precious metal returns to proportions important in solid solution in the ß-NiAl phase of nickel aluminide. It gives both better adhesion to the protective alumina layer (oxidation cyclic) and good environmental resistance by presence of molten salts (hot corrosion).
- alloy coatings are not obtained using processes involving high diffusion temperature between the superalloy substrate and the coating under development.
- an alloy is already deposited on the substrate made of a composition suitable for functionality sought such as resistance to oxidation and hot corrosion.
- the most commonly used alloy coatings for high temperature protection applications for superalloy substrates are type coatings MCrAlY.
- M represents the base alloy which may be cobalt, nickel, iron, or a combination of these three metals.
- Chromium is present between 10 and 40% by mass and is mainly used to increase the resistance of coatings to hot corrosion.
- Aluminum is present in contents between 2 and 25 % by mass. Its major role is the hot forming of a protective layer of alumina which it is desired to be at slow growth, as chemically stable as possible to resist hot corrosion and extremely adherent so as to withstand the stresses of expansion differential during thermal cycling at temperature high.
- Yttrium Y is present at levels between a few tens of ppm and a few percent by mass. His role is twofold:
- Certain other elements such as hafnium, zirconium, cerium, lanthanides and generally most rare earths can play a role very similar to that of yttrium on the adhesion of protective alumina layers.
- the contribution of yttrium and related elements sometimes called active elements, to the effectiveness of protective coatings of superalloys is limited to only high temperature oxidation. No type effect active element could not be highlighted in the case of hot corrosion of coated superalloys.
- a first solution consists of the coatings of Aluminized MCrAlY.
- Aluminization in pack or vapor phase on a MCrAlY coating deposited by one of the techniques mentioned above has the advantage of obtaining a external composition of the coating enriched with aluminum, this which extends the life of the coating, in particular by high temperature oxidation condition.
- a second solution is made up of electrophoretic MCrAlY coatings.
- the process for producing this type of coating is described, for example, in patent FR 2,529,991 filed by SNECMA.
- the method consists in depositing on a substrate made of nickel-based superalloy a coating composed of agglomerated MCrAlY alloy powders, by a suitable electrophoresis technique.
- This porous deposit having no mechanical strength, it is necessary to fill the porosity by aluminization in the vapor phase.
- the aluminization plays the role of consolidation and filling of the pores left between the agglomerated MCrAlY powder grains.
- the final structure is very similar to that of a traditional aluminized MCrAlY coating.
- the slightly directional electrophoretic technique allows evenly form shaped parts complex than turbine distributor vane doublets. This technique is much less expensive than a coating MCrAlY deposited by plasma then aluminized for a quality of equivalent protection. However the coating obtained has a limited performance gain compared to a MCrAlY coating alone.
- This coating has the major drawback of not comprising, by construction, platinum only in its external part. In done, it is the overlay of a coating of MCrAlY traditional and an aluminide coating modified by the platinum.
- the beneficial effects of MCrAlY coatings and platinum modified aluminide coatings are juxtaposed but not added. The synergy of effects does therefore cannot be obtained.
- the total thickness of the coating is at least equal to 100 ⁇ m, which can pose problems with added mass when the coating is performed on rotating parts.
- such coating is, of a very high cost price (at least equal to the sum of the prices of a traditional MCrAlY coating and a platinum modified aluminide).
- the problem coating of complex shaped parts always arises acutely.
- the invention consists in carrying out on the surface of a superalloy a first deposit of an alloy powder agglomerated containing at least chromium, aluminum and a active element, and to fill the open porosity of the deposit of powder by a second electrolytic deposit of precious metal from the platinum mine.
- Appropriate heat treatment is then performed to allow inter-broadcast between the powder-based coating and electrolytic coating and obtain a coating comprising over its entire thickness chromium, an active element such as Yttrium, and a metal precious from the platinum mine.
- thermochemical aluminization treatment can be done in a final step to bring a additional aluminum in the final coating and complete the filling of the residual gaps between grains of powder deposited.
- the invention consists in depositing, at the surface of a superalloy, an agglomerated alloy powder containing at least chromium, aluminum, an element active and at least one precious metal from the platinum mine and to fill the open porosity of the agglomerated powder deposit by an aluminization treatment.
- the deposition of the alloy powder can be carried out by a electrophoretic technique or by painting technique with a thermodegradable or volatile binder.
- the active element is chosen from the group consisting of Yttrium, Yttric or lanthanidic rare earths such that Zr, Hf, La, Ce.
- the element of the platinum mine is chosen from the group consisting of platinum, palladium, Rhodium, Ruthenium, Osmium, Iridium and combinations of these metals.
- the coating is deposited on a sample 10 or a part nickel or cobalt-based superalloy, equiaxial, with directed or monocrystalline solidification, taking the place of substrate, such as for example and without limitation the superalloys known under the names: IN100, DS200, DS186, MAR M 247, DS247, MAR M 509, René 77, René 125, HS31, X40, AM1, AM3.
- composition of these powders can occur without departing from the scope of this invention, such as by example the replacement of all or part of the active element Y by one or more other active elements taken in the following list: Zr, Hf, La, Ce and more generally the yttrique or lanthanidic rare earths.
- the particle size of the powder can be between 2 and 100 micrometers, preferably between 4 and 15 ⁇ m. It is particularly advantageous to use a particle size of fine powder, because it will on the one hand limit the final surface roughness of the coating and on the other hand limit the size of the residual porosities after the electrophoretic deposition. The risk of persistence of porosity in the coating after its final stage of development is finds decreased by the same amount.
- This first deposit can be made using for example a painting technique with thermodegradable binder or volatile, or advantageously an electrophoretic technique.
- the electrophoretic technique consists in carrying out a porous skeleton of metallic powders by immersing the parts to be coated in an insulating solution containing suspension of the powders to be deposited.
- the homogeneity of the suspension is ensured by agitation, which avoids sedimentation of particles at the bottom of the tank electrophoresis.
- the parts to be coated are positioned and cathode polarized.
- the anode consists of an electrode shaped arranged opposite and / or around the part to be coated, in order to obtain a homogeneous distribution of the electric field in the vicinity of the part, and thus the thicknesses of the deposit regular.
- the metallic particles are charged electrically in the electrostratic field and migrate quickly towards the surface of the room where they agglomerate by the Coulomb attraction. Parties not to be coated are protected by masking assemblies made in materials chemically compatible with the bath electrophoresis. Keeping parts in the tank and electrical connections of the parts are also ensured by the assembly comprising the mask (s).
- the difference of potential applied between anode and cathode, ensuring the migration of metallic particles, is between 200 and 500 V.
- the duration of deposit is between 1 second and 1 minute (typically less than 10 seconds) depending on the particle size of the powders to be deposited, and the thickness of the deposit wanted.
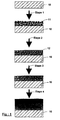
- the deposited coating is not dense, but easily manipulated as shown in FIG. 1.
- the coating thicknesses can be between 20 and 200 ⁇ m at this stage, preferably between 30 and 60 ⁇ m. Depending on the density and particle size of the powder used, this corresponds to a mass of deposited alloy of between 10 and 100 mg / cm 2 , preferably between 20 and 60 mg / cm 2 .
- the second step 2 of the coating production process is a step of electroplating a metal alloy containing at least one platinum mine metal.
- this platinum mine alloy is chosen from pure platinum or a platinum-rhodium alloy, or another palladium-nickel alloy.
- Sample or piece having previously undergone step 1 of the process is immersed in an electrolytic metal or alloy deposition bath selected.
- An anode system and / or current thieves, is arranged around the sample or the part to be coated with so that the distribution of current densities is homogeneous at all points of the room, this using the know-how of a person skilled in the art of electroplating.
- the cathodic current density to be applied is chosen, in depending on the operating parameters of the bath used.
- This current density is sufficiently low, in order to allow the penetration of the electrolytic deposit in all the gaps left between the grains of powder deposited during step 1.
- the duration of the electrolysis is adjusted by so that the mass of precious metal deposited is between 5 and 70%, preferably between 20 and 50% of the total mass of deposits made during steps 1 and 2.
- the coating 12 obtained is composed of the juxtaposition of the MCrAlY powder and the alloy metallic containing at least one platinum mine metal.
- the annealing temperature can be between 750 and 1250 ° C and its duration between 15 minutes and 48 hours (preferably between 2 and 4 p.m.). In the event that none further processing is not planned, it is necessary that the annealing completely closes the residual porosity of the coating and that the interdiffusion between the powder grains of MCrAlY and the deposition of the electrodeposited metal alloy be complete. It is then necessary to apply the highest annealing temperatures and / or durations of anneals the longest. In the event that a treatment later described in step 4 below is planned, the densification of the coating and the interdiffusion between grains of MCrAlY powder and deposition of the alloy metallic electrodeposited is partly ensured by step 4. The temperatures and / or the annealing times can then to be weaker.
- Step 4 of the method according to the invention is optional.
- She consists of aluminizing the coating according to conventional methods known to those skilled in the art. To this end, it is possible to use vapor phase aluminization or aluminization by applying paint aluminizing. It is also possible to apply checkout aluminization techniques.
- This fourth step enriches the aluminum outer surface of the coating, thereby extending the life lifetime of this coating under high oxidation conditions temperature. This fourth step also makes it possible to complete the filling of the interstices left between the grains of powder deposited during the first stage.
- the first deposit made in step 1 is made from an MCrAlY type alloy powder additionally containing one or more metals from the mine of platinum.
- the addition of one or more metals from the platinum mine can be done in different ways. It is possible to directly produce powders whose composition corresponds to the formula MCrAlY + MP where MP is a metal of the platinum mine or an alloy thereof. The techniques of manufacture of such powders are those corresponding to the state of the art in powder metallurgy. It is exhaustively, casting the alloy followed by a atomization step by arc or by rotating electrode. he it is also possible to use MCrALY powders conventional, having undergone a surface treatment subsequent so as to deposit on the periphery of the grains a alloy containing the metal of the MP platinum mine.
- This subsequent surface treatment can be for example a autocatalytic chemical deposit or not, a deposit electrolytic, an organometallic PVD or CVD type deposit.
- MCrALY + MP type powders are further characterized by the metal content of the MP platinum mine.
- the metal of the platinum MP mine can represent between 2 and 60% by mass (preferably between 20 and 50%) relative to the total mass of the powder.
- This first deposit is then directly followed by a deposit coating aluminization according to step 4 of process, steps 2 and 3 being omitted.
- steps 2 and 3 being omitted.
- aluminization depot only aluminization techniques in vapor phase or by application of aluminizing paint can be used. Aluminization techniques in body are not possible because the friction of the powders aluminization cement on a powdery deposit directly from step 1 and not yet consolidated risks destroying the porous layer.
- the coating is carried out on a sample in the form of plates of dimensions 20 ⁇ 30 ⁇ 2 mm 3 made of DS200 + Hf alloy.
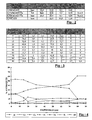
- This sample underwent a first electrophoretic deposition from a powder of CoNiCrAlY alloy, the composition of which is given in the table represented in FIG. 2.
- the particle size of the powder is centered on approximately 15 ⁇ m.
- the quantity of powder deposited corresponds to a mass gain of 15 mg / cm 2 .
- This sample then underwent a second electroplating of Pd-20% mass Ni alloy.
- the current density used for this second deposit is 1 A / dm 2 for a duration of approximately 45 minutes.
- the amount of palladium alloy deposited in this way is approximately 8 mg / cm 2 (or approximately 35% of the metallic mass deposited in total during these first two stages).
- a two-hour secondary vacuum diffusion annealing at 850 ° C was carried out.
- aluminization in the vapor phase using a cement alloy of Cr-30% by mass Al, and an activator of the NH 4 F type was carried out at 1100 ° C. for 10 h.
- the coating obtained is dense, single-phase with a total thickness of approximately 80 ⁇ m. It is essentially composed of a ß (Ni, Co) Al phase containing chromium, palladium and yttrium in solid solution.
- Figures 3 and 4 illustrate the distribution of the main elements in the thickness of the coating.
- the atomic percentages were determined by electron microprobe analysis. Yttrium cannot be validly detected by this type of measurement, but is detected with an electron microscope at higher magnification.
- Figures 3 and 4 show that the composition of the coating varies little in its thickness and in particular that the metal of the platinum mine is present in a significant amount throughout the thickness of the coating.
- Example 1 The procedure is as in Example 1 except during the electrolytic deposition step where the amount of palladium alloy deposited corresponds to 12 mg / cm 2 by increasing the duration of the electrolytic deposition in proportion.
- the mass of the palladium alloy then corresponds to approximately 44% of the metal mass deposited in total during the two deposition operations.
- the structure of the coating obtained is identical to that of Example 1, but the amount of palladium is greater (15 atomic% on average).
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Other Surface Treatments For Metallic Materials (AREA)
- Solid-Phase Diffusion Into Metallic Material Surfaces (AREA)
- Electroplating Methods And Accessories (AREA)
- Turbine Rotor Nozzle Sealing (AREA)
Claims (14)
- Verfahren zur Herstellung einer Schutzbeschichtung gegen Oxidation bei hohen Temperaturen und gegen Hitzekorrosion an Bauteilen aus Superlegierungen,
dadurch gekennzeichnet, daß es darin besteht:in einem ersten Verfahrensschritt auf dem zu beschichtenden Bauteil einen ersten Überzug einer feinpulverigen Legierung, die mindestens Chrom, Aluminium und ein aktives Element enthält und eine offene Restporosität aufweist, aufzubringen,in einem zweiten Verfahrensschritt die offenen Restporen des ersten feinpulverigen Überzugs mit einem zweiten, elektrolytischen, metallischen Überzug, der mindestens ein Platin(gruppen)erz-Metall enthält, geschlossen werden,in einem dritten Verfahrensschritt eine Wärmebehandlung durchzuführen, durch die das Ineinander-Diffundieren des ersten feinpulverigen Überzugs und des zweiten, elektrolytischen Überzugs gewährleistet wird. - Verfahren zur Herstellung einer Schutzbeschichtung nach Anspruch 1, dadurch gekennzeichnet, daß es ferner einen vierten Verfahrensschritt beinhaltet, der darin besteht, ein Aluminieren des in dem dritten Verfahrensschritt erzielten Überzugs dergestalt durchzuführen, daß dieser Überzug mit Aluminium angereichert wird und das Schließen seiner Poren vollendet wird.
- Verfahren zur Herstellung einer Schutzbeschichtung nach Anspruch 1 oder 2, dadurch gekennzeichnet, daß das Platingruppen(erz)-Metall, das im zweiten Verfahrensschritt aufgebracht wird, in einem Masseverhältnis von 5 bis 70 % zur Gesamtmasse der in den beiden ersten Verfahrensschritten hergestellten Überzüge steht.
- Verfahren zur Herstellung einer Schutzbeschichtung nach einem der Ansprüche 1 bis 3, dadurch gekennzeichnet, daß die Wärmebehandlung des dritten Verfahrensschritts bei einer Temperatur von 750 bis 1250 °C und über eine Zeitdauer von 15 Minuten bis 48 Stunden durchgeführt wird.
- Verfahren zur Herstellung einer Schutzbeschichtung gegen Oxidation bei hohen Temperaturen und gegen Hitzekorrosion an Bauteilen aus Superlegierungen, dadurch gekennzeichnet, daß es darin besteht:in einem ersten Verfahrensschritt auf dem zu beschichtenden Bauteil einen ersten Überzug einer feinpulverigen Legierung, die mindestens Chrom, Aluminium und ein aktives Element sowie mindestens ein Platingruppen(erz)-Metall enthält und eine offene Restporosität aufweist, aufzubringen,in einem zweiten Verfahrensschritt ein Aluminieren des in dem ersten Verfahrensschritt erzielten Überzugs dergestalt durchzuführen, daß dieser Überzug mit Aluminium angereichert wird und die offenen Restporen des ersten feinpulverigen Überzugs geschlossen werden.
- Verfahren zur Herstellung einer Schutzbeschichtung nach Anspruch 5, dadurch gekennzeichnet, daß das Platingruppen(erz)-Metall in einem Masseverhältnis von 2 bis 60 % zur Gesamtmasse des Pulvers steht.
- Verfahren zur Herstellung einer Schutzbeschichtung nach einem der vorherigen Ansprüche, dadurch gekennzeichnet, daß der Überzug aus einer feinpulverigen Legierung durch eine Elektrophorese-Technik hergestellt wird.
- Verfahren zur Herstellung einer Schutzbeschichtung nach einem der Ansprüche 1 bis 6, dadurch gekennzeichnet, daß der Überzug aus einer feinpulverigen Legierung durch eine Anstrich-Technik mit einem durch Wärme abbaubaren oder flüchtigen Binder hergestellt wird.
- Verfahren zur Herstellung einer Schutzbeschichtung nach einem der vorherigen Ansprüche, dadurch gekennzeichnet, daß das aktive Element der feinpulverigen Legierung aus einer Gruppe gewählt wird, die Yttrium, seltene Yttererden und seltene Lanthaniderden umfaßt.
- Verfahren zur Herstellung einer Schutzbeschichtung nach einem der vorherigen Ansprüche, dadurch gekennzeichnet, daß das Platingruppen(erz)-Metall aus einer Gruppe gewählt wird, die Platin, Palladium, Rhodium, Ruthenium, Osmium, Iridium sowie Verbindungen dieser Metalle umfaßt.
- Schutzbeschichtung, die mit dem Herstellungsverfahren nach einem der Ansprüche 1 bis 4 hergestellt ist, dadurch gekennzeichnet, daß sie mindestens die Elemente Cr, Al, ein aktives Element und ein Platingruppen(erz)-Metall enthält, wobei diese Elemente alle in der gesamten Dicke der Beschichtung zusammen vorhanden sind.
- Schutzbeschichtung, die mit dem Herstellungsverfahren nach einem der Ansprüche 5 oder 6 hergestellt ist, dadurch gekennzeichnet, daß sie mindestens die Elemente Cr, Al, ein aktives Element und ein Platingruppen(erz)-Metall enthält, wobei diese Elemente alle in der gesamten Dicke der Beschichtung zusammen vorhanden sind.
- Schutzbeschichtung nach einem der Ansprüche 11 oder 12, dadurch gekennzeichnet, daß sie als Wärmesperr-Unterschicht für ein Bauteil aus Superlegierung verwendet wird.
- Bauteil aus Superlegierung, dadurch gekennzeichnet, daß es eine Schutzbeschichtung nach einem der Ansprüche 11 oder 12 aufweist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9615257 | 1996-12-12 | ||
| FR9615257A FR2757181B1 (fr) | 1996-12-12 | 1996-12-12 | Procede de realisation d'un revetement protecteur a haute efficacite contre la corrosion a haute temperature pour superalliages, revetement protecteur obtenu par ce procede et pieces protegees par ce revetement |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0848079A1 EP0848079A1 (de) | 1998-06-17 |
| EP0848079B1 true EP0848079B1 (de) | 2000-03-15 |
Family
ID=9498582
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP97402999A Expired - Lifetime EP0848079B1 (de) | 1996-12-12 | 1997-12-11 | Verfahren zur Herstellung einer Schutzbeschichtung mit grosser Wirksamkeit gegen Hochtemperatur-Verschleiss von Superlegierungen, Schutzbeschichtung und damit beschichtete Teile |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US6183888B1 (de) |
| EP (1) | EP0848079B1 (de) |
| JP (1) | JP3431474B2 (de) |
| CA (1) | CA2228768C (de) |
| DE (1) | DE69701442T2 (de) |
| FR (1) | FR2757181B1 (de) |
Families Citing this family (31)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2745590B1 (fr) * | 1996-02-29 | 1998-05-15 | Snecma | Revetement de barriere thermique a sous-couche amelioree et pieces revetues par une telle barriere thermique |
| DE19807636C1 (de) * | 1998-02-23 | 1999-11-18 | Mtu Muenchen Gmbh | Verfahren zum Herstellen einer korrosions- und oxidationsbeständigen Schlickerschicht |
| FR2787472B1 (fr) * | 1998-12-16 | 2001-03-09 | Onera (Off Nat Aerospatiale) | Procede pour produire une poudre d'alliage metallique de type mcraly et revetements obtenus avec cette poudre |
| DE59909337D1 (de) * | 1999-06-03 | 2004-06-03 | Alstom Technology Ltd Baden | Verfahren zur Herstellung oder zur Reparatur von Kühlkanälen in einstristallinen Komponenten von Gasturbinen |
| SE516045C2 (sv) * | 2000-03-20 | 2001-11-12 | Westinghouse Atom Ab | Komponent innefattande en zirkoniumlegering, förfarande för att tillverka nämnda komponent samt en nukleär anläggning innefattande nämnda komponent |
| FR2827311B1 (fr) * | 2001-07-12 | 2003-09-19 | Snecma Moteurs | Procede de reparation locale de pieces revetues d'une barriere thermique |
| US6838190B2 (en) * | 2001-12-20 | 2005-01-04 | General Electric Company | Article with intermediate layer and protective layer, and its fabrication |
| US7371467B2 (en) | 2002-01-08 | 2008-05-13 | Applied Materials, Inc. | Process chamber component having electroplated yttrium containing coating |
| DE60231084D1 (de) * | 2002-12-06 | 2009-03-19 | Alstom Technology Ltd | Verfahren zur selektiven Abscheidung einer MCrAlY-Beschichtung |
| US7297247B2 (en) * | 2003-05-06 | 2007-11-20 | Applied Materials, Inc. | Electroformed sputtering target |
| US20050028248A1 (en) * | 2003-08-08 | 2005-02-10 | Yan Suen Ching | Multi-axially stretchable fabric cap |
| DE10355234A1 (de) * | 2003-11-26 | 2005-06-30 | Mtu Aero Engines Gmbh | Verfahren zum Herstellen einer korrosionsbeständigen und oxidationsbeständigen Beschichtung sowie Bauteil mit einer solchen Beschichtung |
| US7604726B2 (en) * | 2004-01-07 | 2009-10-20 | Honeywell International Inc. | Platinum aluminide coating and method thereof |
| US20070104886A1 (en) * | 2005-11-10 | 2007-05-10 | General Electric Company | Electrostatic spray for coating aircraft engine components |
| KR100855531B1 (ko) * | 2004-04-13 | 2008-09-01 | 어플라이드 머티어리얼스, 인코포레이티드 | 전기 도금된 이트륨 함유 코팅을 갖는 프로세스 챔버 요소 |
| US7645485B2 (en) * | 2004-04-30 | 2010-01-12 | Honeywell International Inc. | Chromiumm diffusion coatings |
| FR2870858B1 (fr) * | 2004-05-28 | 2007-04-06 | Snecma Moteurs Sa | Procede de fabrication ou de reparation d'un revetement sur un substrat metallique |
| US7229701B2 (en) * | 2004-08-26 | 2007-06-12 | Honeywell International, Inc. | Chromium and active elements modified platinum aluminide coatings |
| NL1028629C2 (nl) * | 2005-03-24 | 2006-10-02 | Netherlands Inst For Metals Re | Bekledingslaag, substraat voorzien van een bekledingslaag en werkwijze voor het aanbrengen van een corrosiewerende bekledingslaag. |
| US20070138019A1 (en) * | 2005-12-21 | 2007-06-21 | United Technologies Corporation | Platinum modified NiCoCrAlY bondcoat for thermal barrier coating |
| CA2635481C (en) | 2005-12-28 | 2013-08-13 | Ansaldo Energia S.P.A. | Alloy composition for the manufacture of protective coatings, its use, process for its application and super-alloy articles coated with the same composition |
| US8137820B2 (en) * | 2006-02-24 | 2012-03-20 | Mt Coatings, Llc | Roughened coatings for gas turbine engine components |
| US20080080978A1 (en) * | 2006-10-03 | 2008-04-03 | Robert George Zimmerman | Coated turbine engine components and methods for making the same |
| US7767072B2 (en) * | 2006-12-15 | 2010-08-03 | Honeywell International Inc. | Method of forming yttrium-modified platinum aluminide diffusion coating |
| US8124246B2 (en) * | 2008-11-19 | 2012-02-28 | Honeywell International Inc. | Coated components and methods of fabricating coated components and coated turbine disks |
| RU2542870C2 (ru) | 2009-05-26 | 2015-02-27 | Сименс Акциенгезелльшафт | Слоистая система покрытия со слоем mcralx и слоем, богатым по хрому, и способ ее получения |
| CN102449742B (zh) * | 2009-05-27 | 2015-12-09 | 诺发系统有限公司 | 用于在薄籽晶层上进行电镀的脉冲序列 |
| US9385035B2 (en) | 2010-05-24 | 2016-07-05 | Novellus Systems, Inc. | Current ramping and current pulsing entry of substrates for electroplating |
| US8367160B2 (en) | 2010-11-05 | 2013-02-05 | United Technologies Corporation | Coating method for reactive metal |
| PL3612660T3 (pl) | 2017-04-21 | 2022-07-18 | Oerlikon Surface Solutions Ag, Pfäffikon | Powłoka wiążąca PVD |
| JP7713456B2 (ja) | 2020-01-10 | 2025-07-25 | ラム リサーチ コーポレーション | Tsv処理窓ならびに長いパルス出力および傾斜部形成による充填性能強化 |
Family Cites Families (17)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE1796175C2 (de) * | 1968-09-14 | 1974-05-30 | Deutsche Edelstahlwerke Gmbh, 4150 Krefeld | Hochtemperaturkorrosions- und zunderbeständige Diffusionsschutzschicht auf Gegenständen aus hochwarmfesten Legierungen auf Nickel- und/oder Kobaltbasis |
| BE757636A (fr) * | 1969-11-03 | 1971-04-01 | Deutsche Edelstahlwerke Ag | Procede de protection en surface pour objets metalliques |
| US3874901A (en) * | 1973-04-23 | 1975-04-01 | Gen Electric | Coating system for superalloys |
| US4145481A (en) * | 1977-08-03 | 1979-03-20 | Howmet Turbine Components Corporation | Process for producing elevated temperature corrosion resistant metal articles |
| US4123594A (en) * | 1977-09-22 | 1978-10-31 | General Electric Company | Metallic coated article of improved environmental resistance |
| US4123595A (en) * | 1977-09-22 | 1978-10-31 | General Electric Company | Metallic coated article |
| JPS5582760A (en) * | 1978-12-15 | 1980-06-21 | Hitachi Ltd | Coating method for platinum group metal onto heat resistant alloy |
| FR2529911B1 (fr) * | 1982-07-08 | 1986-05-30 | Snecma | Procede et dispositif pour la realisation de revetements protecteurs metalliques |
| FR2559508B1 (fr) * | 1984-02-15 | 1992-12-24 | Snecma | Procede de protection des alliages resistant a chaud notamment a base de nickel |
| US4714624A (en) * | 1986-02-21 | 1987-12-22 | Textron/Avco Corp. | High temperature oxidation/corrosion resistant coatings |
| FR2638174B1 (fr) * | 1988-10-26 | 1991-01-18 | Onera (Off Nat Aerospatiale) | Procede de protection de surface de pieces metalliques contre la corrosion a temperature elevee, et piece traitee par ce procede |
| DE3918380A1 (de) * | 1989-06-06 | 1990-12-20 | Starck Hermann C Fa | Hochtemperatur-verbund-werkstoff, verfahren zu seiner herstellung sowie dessen verwendung |
| GB9218858D0 (en) * | 1992-09-05 | 1992-10-21 | Rolls Royce Plc | High temperature corrosion resistant composite coatings |
| GB9302978D0 (en) * | 1993-02-15 | 1993-03-31 | Secr Defence | Diffusion barrier layers |
| US5495386A (en) * | 1993-08-03 | 1996-02-27 | Avx Corporation | Electrical components, such as capacitors, and methods for their manufacture |
| US5427866A (en) * | 1994-03-28 | 1995-06-27 | General Electric Company | Platinum, rhodium, or palladium protective coatings in thermal barrier coating systems |
| GB9426257D0 (en) * | 1994-12-24 | 1995-03-01 | Rolls Royce Plc | Thermal barrier coating for a superalloy article and method of application |
-
1996
- 1996-12-12 FR FR9615257A patent/FR2757181B1/fr not_active Expired - Fee Related
-
1997
- 1997-12-03 CA CA002228768A patent/CA2228768C/fr not_active Expired - Fee Related
- 1997-12-11 EP EP97402999A patent/EP0848079B1/de not_active Expired - Lifetime
- 1997-12-11 DE DE69701442T patent/DE69701442T2/de not_active Expired - Lifetime
- 1997-12-11 US US08/989,059 patent/US6183888B1/en not_active Expired - Lifetime
- 1997-12-12 JP JP34321197A patent/JP3431474B2/ja not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| DE69701442D1 (de) | 2000-04-20 |
| EP0848079A1 (de) | 1998-06-17 |
| JPH10176283A (ja) | 1998-06-30 |
| US6183888B1 (en) | 2001-02-06 |
| FR2757181A1 (fr) | 1998-06-19 |
| JP3431474B2 (ja) | 2003-07-28 |
| CA2228768C (fr) | 2005-02-15 |
| FR2757181B1 (fr) | 1999-02-12 |
| DE69701442T2 (de) | 2000-09-07 |
| CA2228768A1 (fr) | 1998-06-12 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2228768C (fr) | Procede de realisation d'un revetement protecteur a haute efficacite contre la corrosion a haute temperature pour superalliages, revetement protecteur obtenu par ce procede et pieces protegees par ce revetement | |
| EP0792948B1 (de) | Wärmehemmende Beschichtung mit verbesserter Unterschicht und Gegenstände mit dieser Wärmehemmende Beschichtung | |
| US7157151B2 (en) | Corrosion-resistant layered coatings | |
| US6372299B1 (en) | Method for improving the oxidation-resistance of metal substrates coated with thermal barrier coatings | |
| CA2051839C (en) | Method of forming platinum-silicon-enriched diffused aluminide coating on a superalloy substrate | |
| CZ20004537A3 (cs) | Vícevrstvový vazební povlak pro povlakový systém tepelné ochranné bariéry a způsob jeho vytvoření | |
| JPH06220607A (ja) | 高温耐腐食性複合被覆 | |
| EP2459780B1 (de) | Stück aus einem substrat mit einer auf der basis einer ceriumoxid keramischen beschichtung | |
| EP3538500A1 (de) | Mit einer wärmedämmung beschichtetes turbomaschinenteil und verfahren zur herstellung davon | |
| US20080166548A1 (en) | Coating material for thermal barrier coating having excellent corrosion resistance and heat resistance and method of producing the same | |
| EP0990716B1 (de) | Wärmedämmschicht | |
| EP3377680B1 (de) | Flugzeugtriebwerksteil mit einer erosionsschutzschicht und verfahren zur herstellung solch eines teils | |
| CA2769198C (fr) | Methode de fabrication d'une barriere thermique | |
| FR2718464A1 (fr) | Article en super alliage ayant un revêtement de barrière thermique et sa fabrication. | |
| EP1141442A1 (de) | Verfahren zur herstellung eines metallegierungspulvers vom typ mcraly und nach diesem verfahren erhaltene überzüge | |
| FR2813318A1 (fr) | Formation d'un revetement aluminiure incorporant un element reactif, sur un substrat metallique | |
| WO2015007983A2 (fr) | Procede de fabrication d'une sous-couche metallique a base de platine sur un substrat metallique | |
| WO2012146864A1 (fr) | Pièce comportant un revêtement sur un substrat métallique en superalliaae, le revêtement comprenant une sous-couche métallique | |
| WO2019077271A1 (fr) | Piece de turbine en superalliage comprenant du rhenium et procede de fabrication associe | |
| CA2508821C (fr) | Procede de fabrication ou de reparation d'un revetement sur un substrat metallique | |
| US20080080978A1 (en) | Coated turbine engine components and methods for making the same |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19971222 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE FR GB IT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AKX | Designation fees paid |
Free format text: DE FR GB IT SE |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): DE FR GB IT SE |
|
| 17Q | First examination report despatched |
Effective date: 19990322 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| RTI1 | Title (correction) |
Free format text: METHOD FOR DEPOSITING A PROTECTIVE COATING WITH GREAT EFFICIENCY AGAINST CORROSION AT HIGH TEMPERATURES FOR SUPERALLOYS, PROTECTIVE COATING AND PIECES PROTECTED WITH SUCH A COATING |
|
| RTI1 | Title (correction) |
Free format text: METHOD FOR DEPOSITING A PROTECTIVE COATING WITH GREAT EFFICIENCY AGAINST CORROSION AT HIGH TEMPERATURES FOR SUPERALLOYS, PROTECTIVE COATING AND PIECES PROTECTED WITH SUCH A COATING |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB IT SE |
|
| REF | Corresponds to: |
Ref document number: 69701442 Country of ref document: DE Date of ref document: 20000420 |
|
| ITF | It: translation for a ep patent filed | ||
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20000410 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: TP Ref country code: FR Ref legal event code: CD |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E Free format text: REGISTERED BETWEEN 20120517 AND 20120523 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20151125 Year of fee payment: 19 Ref country code: DE Payment date: 20151119 Year of fee payment: 19 Ref country code: IT Payment date: 20151120 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20151124 Year of fee payment: 19 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20161205 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 69701442 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20161211 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161212 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161211 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170701 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161211 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD Owner name: SAFRAN AIRCRAFT ENGINES, FR Effective date: 20170717 |