EP0887130B1 - Im Druckgiessverfahren gefertigtes Maschinengehäuse, insbesondere für Brennkraftmaschinen - Google Patents
Im Druckgiessverfahren gefertigtes Maschinengehäuse, insbesondere für Brennkraftmaschinen Download PDFInfo
- Publication number
- EP0887130B1 EP0887130B1 EP98107786A EP98107786A EP0887130B1 EP 0887130 B1 EP0887130 B1 EP 0887130B1 EP 98107786 A EP98107786 A EP 98107786A EP 98107786 A EP98107786 A EP 98107786A EP 0887130 B1 EP0887130 B1 EP 0887130B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- insertion part
- insert
- mandrel
- internal combustion
- combustion engines
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000002485 combustion reaction Methods 0.000 title claims 2
- 238000004512 die casting Methods 0.000 claims description 7
- 238000000034 method Methods 0.000 claims description 5
- 239000002184 metal Substances 0.000 claims description 3
- 229910001092 metal group alloy Inorganic materials 0.000 claims description 3
- 238000003780 insertion Methods 0.000 claims 7
- 230000037431 insertion Effects 0.000 claims 7
- 239000000446 fuel Substances 0.000 claims 2
- 238000005192 partition Methods 0.000 claims 1
- 238000009825 accumulation Methods 0.000 description 5
- 238000005266 casting Methods 0.000 description 5
- 239000000463 material Substances 0.000 description 5
- 238000000926 separation method Methods 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D19/00—Casting in, on, or around objects which form part of the product
- B22D19/0009—Cylinders, pistons
Definitions
- the invention is based on the teaching GB-2 248 203 A.
- This document shows and describes the arrangement of Bushings in a T-piece formed from pipe sections by casting, the Before the casting of the T-piece, bushings are arranged on the fly in the casting mold Thorns are positioned.
- the invention is based on the object for a die casting process Machine housing a serving to reduce material accumulation To show insert.
- a perfectly adapted to the given designs of the machine housing Chamber is further advantageously achieved in that the insert with Internal pressure has molded projections. This can lead to a material accumulation can be optimally reduced.
- this is made from a light metal alloy cast insert molded into a light metal machine housing, the insert with its extensions in a cylinder crankcase especially in the area near the cylinder liner in the machine housing serves to reduce material accumulation.
- An operating medium channel with connecting lines arranged on the outside of the housing the cylinder head arranged above is e.g. from the FR 2 225 628 A known.
- the invention is for one in the Described machine housing shown.
- This mandrel 4 can only with a short insert 2, 2 'and / or low weight be arranged on one side in the die-casting mold, with long insert 2, 2 ' and / or heavy weight, the mandrel 4 can have a securing pin at its free end 5 have, which engages in a slide of the die.
- the chamber 3 formed by the insert 2 is on the tubular Insert 2 shaped hollow extensions 7 volume increased.
- This increase in volume the insert 2 is preferably achieved in that the Insert 2 has projections 7 molded with internal high pressure.
- Positioning of this insert 2 has this in an end region a fixing profile 8 which interacts positively with the mandrel 4, e.g. on Square.
- this is formed from a light metal alloy Insert 2, 2 'cast into a light metal machine housing 1, 1', the insert 2 with its extensions 7 in a cylinder crankcase 9 serves the advantageous reduction of material accumulation.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Cylinder Crankcases Of Internal Combustion Engines (AREA)
Description
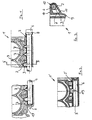
- Figur 1
- ein Zylinder-Kurbelgehäuse mit innenhochdruckverformtem Einlegeteil,
- Figur 2
- das verformte Einlegeteil als Betriebsmittelkanal im Schnitt gemäß der Linie II-II, und
- Figur 3
- ein rohrförmiges Einlegeteil.
Claims (4)
- Im Druckgieß-Verfahren gefertigtes Maschinengehäuse, insbesondere für Brennkraftmaschinen,dadurch gekennzeichnet,das eine mittels eines hohlen Einlegeteiles (2) ausgebildete Kammer (3) aufweist, wobeidas in einer Druckgussform auf einem im wesentlichen fliegend angeordneten Dorn (4) positionierte Einlegeteil (2) längs seiner Erstreckung über seine Innenkontur mit einem im wesentlichen entsprechend angepassten Dorn (4) lagefixiert ist,dass das Einlegeteil (2) die Kammer (3) volumenvergrößernde Fortsätze (7) aufweist, wobeidas Einlegeteil (2) in einem Endbereich ein mit dem Dorn (4) formschlüssig zusammenwirkendes Fixierprofil (8) aufweist.
- Maschinengehäuse nach Anspruch 1, dadurch gekennzeichnet, dass das Einlegeteil (2) mit Innenhochdruck ausgeformte Fortsätze (7) aufweist.
- Maschinengehäuse nach Anspruch 1 oder 2, dadurch gekennzeichnet,dass das Einlegeteil (2) aus einer Leichtmetall-Legierung gebildet undin ein Leichtmetall-Maschinengehäuse (1) eingegossen ist.
- Maschinengehäuse nach einem oder mehreren der Anprüche 1 bis 3, dadurch gekennzeichnet,dass das Einlegeteil (2) in einem an einem Zylinder-Kurbelgehäuse (9) außenseitig und einer Trennfläche (10) zu einem Zylinderkopf benachbart angeordneten Fortsatz (11) einen Betriebsmittelkanal (12) bildet, derggf. mit zum Zylinderkopf gerichteten Verbindungsleitungen (13) ausgebildet ist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19727566A DE19727566A1 (de) | 1997-06-28 | 1997-06-28 | Verfahren zum Druckgießen eines Maschinengehäuses, insbesondere für Brennkraftmaschinen |
| DE19727566 | 1997-06-28 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0887130A1 EP0887130A1 (de) | 1998-12-30 |
| EP0887130B1 true EP0887130B1 (de) | 2002-09-11 |
Family
ID=7833959
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98107786A Expired - Lifetime EP0887130B1 (de) | 1997-06-28 | 1998-04-29 | Im Druckgiessverfahren gefertigtes Maschinengehäuse, insbesondere für Brennkraftmaschinen |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP0887130B1 (de) |
| DE (2) | DE19727566A1 (de) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102005018200A1 (de) * | 2005-04-19 | 2006-11-02 | Honsel Gmbh & Co Kg | Verfahren zum Gießen von Monoblock-Zylinderkurbelgehäusen und Druckgießanlage zur Durchführung des Verfahrens |
| US7921901B2 (en) * | 2008-04-16 | 2011-04-12 | GM Global Technology Operations LLC | Sacrificial sleeves for die casting aluminum alloys |
| US7814879B2 (en) | 2008-04-23 | 2010-10-19 | Techtronic Outdoor Products Technology Limited | Monolithic block and valve train for a four-stroke engine |
| MX2012008451A (es) * | 2010-01-20 | 2012-08-15 | Magna Int Inc | Componente bimetalico y metodo para fabricar el mismo. |
Family Cites Families (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1468508A (en) * | 1973-04-12 | 1977-03-30 | Perkins Engines Ltd | Engine cooling system |
| JPS5429108U (de) * | 1977-07-30 | 1979-02-26 | ||
| DE2904167C2 (de) * | 1979-02-03 | 1982-07-08 | Bayerische Motoren Werke AG, 8000 München | Im Druckgießverfahren herstellbarer Zylinderkopf für wassergekühlte Brennkraftmaschinen |
| DE3013745C2 (de) * | 1980-04-10 | 1982-03-25 | Zahnradfabrik Friedrichshafen Ag, 7990 Friedrichshafen | Gußteil mit Kanälen, sowie Verfahren und Gießform für die Herstellung dieses Gußteils |
| DE3642978C1 (en) * | 1986-12-17 | 1988-06-16 | Bayerische Motoren Werke Ag | Method for the production of holes |
| DE3804801A1 (de) * | 1988-02-16 | 1989-08-24 | Audi Ag | Verfahren zur herstellung von leichtmetall-gussteilen |
| US4913217A (en) * | 1989-01-23 | 1990-04-03 | Farley, Inc. | Locators for expendable core in die casting die |
| DE3932562A1 (de) * | 1989-09-29 | 1991-04-11 | Kolbenschmidt Ag | Vorrichtung zur herstellung von leichtmetallkolben fuer verbrennungskraftmaschinen |
| GB2248203A (en) * | 1990-08-14 | 1992-04-01 | Reilly Royalties Ltd | Improvements to castings |
| DE4128544C2 (de) * | 1990-09-06 | 1999-08-12 | Volkswagen Ag | Verfahren zum Herstellen eines Zylinderkopfes mit einem Portliner |
| DE4102358C2 (de) * | 1991-01-26 | 2000-05-11 | Volkswagen Ag | Im Druckgußverfahren herzustellendes Formteil, Verfahren zur Herstellung des Formteils sowie Hohlkörper zur Einlage in das Formteil |
| JPH0671409A (ja) * | 1992-08-28 | 1994-03-15 | Ryobi Ltd | 水冷シリンダブロック鋳造用金型 |
| DE4314727A1 (de) * | 1993-05-04 | 1994-11-10 | Knorr Bremse Ag | Verfahren zum Herstellen einer Kurbelwelle |
| DE19518417A1 (de) * | 1995-05-19 | 1996-11-21 | Kloeckner Humboldt Deutz Ag | Gegossenes, flüssigkeitsgekühltes Zylinderkurbelgehäuse |
| JP3016364B2 (ja) * | 1995-12-04 | 2000-03-06 | トヨタ自動車株式会社 | 内燃機関のシリンダブロック製造方法 |
-
1997
- 1997-06-28 DE DE19727566A patent/DE19727566A1/de not_active Withdrawn
-
1998
- 1998-04-29 DE DE59805477T patent/DE59805477D1/de not_active Expired - Lifetime
- 1998-04-29 EP EP98107786A patent/EP0887130B1/de not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| EP0887130A1 (de) | 1998-12-30 |
| DE59805477D1 (de) | 2002-10-17 |
| DE19727566A1 (de) | 1999-01-07 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE102005058204B4 (de) | Kühlvorrichtung für eine Verbrennungskraftmaschine | |
| DE19600566C1 (de) | Zylinderkurbelgehäuse einer mehrzylindrigen Brennkraftmaschine | |
| EP2113319B1 (de) | Gießkern zur Bildung eines Kühlkanals | |
| DE102004052788A1 (de) | Zylinderkopfdichtung zum Einsatz in einer Brennkraftmaschine und damit ausgerüstete Brennkraftmaschine | |
| DE10352244A1 (de) | Verfahren zur Herstellung eines Kolbens für einen Verbrennungsmotor | |
| DE60300883T2 (de) | Zylinderkopf einer Brennkraftmaschine und ein Verfahren selbigen herzustellen | |
| DE102009059057A1 (de) | Baueinheit aus Zylinderlaufbuchse und Kurbelgehäuse | |
| EP1884647A2 (de) | Flüssigkeitsgekühlter Zylinderkopf für eine Brennkraftmaschine | |
| EP1570167B1 (de) | Gegossenes bauteil für eine brennkraftmaschine | |
| DE10304971B4 (de) | Gegossenes Bauteil für eine Brennkraftmaschine | |
| DE102005014756A1 (de) | Kühlstruktur für einen Zylinderblock | |
| AT521945B1 (de) | Brennkraftmaschine mit einem Kühlflüssigkeitsmantel | |
| EP0883740B1 (de) | Brennkraftmaschine und verfahren zu deren herstellung | |
| DE102011105388A1 (de) | Kern für ein Gießwerkzeug | |
| EP2832980A1 (de) | Motorgehäuse einer Brennkraftmaschine sowie damit ausgestattete Brennkraftmaschine | |
| DE69719375T2 (de) | Kern und verfahren zum formen eines brennkraftmaschinenzylinderkopfes | |
| DE10232528B4 (de) | Magnetventil mit Ölfilter für variable Nockenwellensteuerung | |
| DE102006034341A1 (de) | Verfahren zum Herstellen eines gegossenen Bauteils mit einem eingegossenen Rohr | |
| DE19813745B4 (de) | Herstellungsverfahren für einen Zylinderkopf eines Verbrennungsmotors | |
| DE112004002493T5 (de) | Vereinfachte Motorarchitektur und Motorbaugruppe | |
| EP1972772B1 (de) | Zylinderkopf für eine flüssigkeitsgekühlte Brennkraftmaschine | |
| DE3447579C2 (de) | ||
| DE10108729B4 (de) | Zylinderkopf einer Brennkraftmaschine mit einem Strömungskanal | |
| DE19734007A1 (de) | Zylinderkopf zur Verwendung für Kurbelgehäuse mit unterschiedlichen Zylinderbohrungsdurchmessern | |
| DE19727566A1 (de) | Verfahren zum Druckgießen eines Maschinengehäuses, insbesondere für Brennkraftmaschinen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE FR GB IT |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 19990619 |
|
| AKX | Designation fees paid |
Free format text: DE FR GB IT |
|
| 17Q | First examination report despatched |
Effective date: 20000406 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| RTI1 | Title (correction) |
Free format text: PRESSURE DIE CAST ENGINE HOUSING, IN PARTICULAR FOR INTERNAL COMBUSTION ENGINES |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB IT |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20020911 |
|
| REF | Corresponds to: |
Ref document number: 59805477 Country of ref document: DE Date of ref document: 20021017 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20030612 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 18 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: CA39 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20150430 Year of fee payment: 18 Ref country code: DE Payment date: 20150411 Year of fee payment: 18 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20150428 Year of fee payment: 18 Ref country code: FR Payment date: 20150430 Year of fee payment: 18 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 59805477 Country of ref document: DE |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20160429 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20161230 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160502 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160429 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160429 |