EP0909620A2 - Presse continue pour le pressage de nattes en panneaux - Google Patents
Presse continue pour le pressage de nattes en panneaux Download PDFInfo
- Publication number
- EP0909620A2 EP0909620A2 EP98117030A EP98117030A EP0909620A2 EP 0909620 A2 EP0909620 A2 EP 0909620A2 EP 98117030 A EP98117030 A EP 98117030A EP 98117030 A EP98117030 A EP 98117030A EP 0909620 A2 EP0909620 A2 EP 0909620A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- press
- inlet
- plate
- plates
- differential
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B5/00—Presses characterised by the use of pressing means other than those mentioned in the preceding groups
- B30B5/04—Presses characterised by the use of pressing means other than those mentioned in the preceding groups wherein the pressing means is in the form of an endless band
- B30B5/06—Presses characterised by the use of pressing means other than those mentioned in the preceding groups wherein the pressing means is in the form of an endless band co-operating with another endless band
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B27—WORKING OR PRESERVING WOOD OR SIMILAR MATERIAL; NAILING OR STAPLING MACHINES IN GENERAL
- B27N—MANUFACTURE BY DRY PROCESSES OF ARTICLES, WITH OR WITHOUT ORGANIC BINDING AGENTS, MADE FROM PARTICLES OR FIBRES CONSISTING OF WOOD OR OTHER LIGNOCELLULOSIC OR LIKE ORGANIC MATERIAL
- B27N3/00—Manufacture of substantially flat articles, e.g. boards, from particles or fibres
- B27N3/08—Moulding or pressing
- B27N3/24—Moulding or pressing characterised by using continuously acting presses having endless belts or chains moved within the compression zone
Definitions
- the invention relates to a continuous press for pressing pressed material mats into pressed material boards in the course of the production of chipboard, fiberboard and other wood-based panels, with press lower part and press upper part, in the press lower part and press upper part, endlessly rotating steel press belts, and with an inlet mouth, wherein a heatable press plate is arranged in the lower press part and in the upper press part and adjoin the press plates protruding heatable inlet plates to form the inlet mouth, furthermore the steel sheet press belts are supported on the press plates and inlet plates with the interposition of rolling elements, in addition a device for adjusting the Inlet mouth and at least one device for adjusting the inlet contour of the inlet mouth are provided.
- Such a press is known in which the Device for setting the inlet contour one Has contour slide on one of the concerned Guide plate associated press spar guided and with With the help of an inlet contour actuator in the inlet direction is adjustable.
- the inlet contour slide points to Inlet plate a plurality of transverse to the direction of entry trending steps that one belong to the contour-defining support staircase.
- Of the Support stairs are assigned at least one counter bar, which is connected to the inlet plate in question.
- the counter bar can be selected against one of the levels of Support stairs can be created.
- the Inlet edges of the inlet mouth to different adjust operational conditions.
- it is Adjustment of the bending lines of the inlet plate concerned only gradually and consequently in limited areas possible, with only a trumpet-shaped Enema mouth can be realized (see. DE 44 33 641).
- a continuous press is also known at which is the top of the two heated inlet plates divided into plate sections to form joints is, so that the inlet contour of the inlet mouth in the Hinge areas has kinks. This also applies to the transition area between the upper inlet plate and the subsequent upper press plate.
- This known embodiment is by means of hydraulic Actuators only the angular position of the plate sections adjusted around the axes of rotation of the joints. Especially problematic is the fact that the assigned Sheet steel press belt when driving over the kinks experiences corresponding bends and consequently one is subject to immediate wear and tear (see DE 195 18 879).
- the invention has for its object a continuous Press the described above
- To create embodiment in which the Inlet contour of the inlet mouth is stepless under generation can set any continuous bending lines and even an almost parallel position from the top inlet plate and lower inlet plate up to the neutral zero line of the press inlet also for pressing extremely thin pressed material mats to perfect pressed material plates under Consideration of high production speeds is adjustable.
- the invention solves this problem with a generic one continuous press in that the device for Setting the inlet contour a plurality of Cylinder piston assemblies that the cylinder piston assemblies in a predetermined distribution on the one hand to the upper and / or lower inlet plate, on the other hand to the Upper press part and / or lower press part are articulated, and that the cylinder piston assemblies to a computer-controlled or -controlled hydraulic system connected are.
- the cylinder piston arrangements are preferably around double-acting differential cylinders.
- the upper inlet plate has a bending radius to the effect that between the upper Inlet plate and the lower inlet plate an almost Parallel position is reached, which extends up to extends below the neutral zero line of the press inlet. Almost parallel location means that a slight taper for running in and lightly clamping the relevant Pressed mat is set.
- the enema mouth or his Inlet contour can also within the scope of the invention as before for the production of thick pressed boards in the previous mode of operation set trumpet-shaped be such that the compression from above and done almost evenly at the bottom. -
- the setting of the Inlet contour depends on the pressing mats and especially the mat thickness.
- the mat values for the suitable bending lines or Bending radii of the upper and, if necessary, lower inlet plate can be done using a conventional path measurement technique record and send it to a computer.
- This calculator determines the necessary correction values and influences the hydraulic control or regulation of the differential cylinder in such a way that the inlet plate in question or plates in the desired by tensile and compressive forces Be brought into shape.
- the differential cylinders are preferred in longitudinal rows and possibly transverse rows on the top and / or articulated lower inlet plate and have the inlet plates in the longitudinal direction of the board or in the direction of entry running channels for the heating medium.
- the invention is based on the knowledge that longitudinally drilled inlet plates in the course of adjustment the bending lines or bending radii of the differential cylinders generated bending moments as opposed to transverse drilled inlet plates taking into account the occurring voltage states take up much cheaper can.
- the invention provides that the Differential cylinder gimbal on the upper and / or lower inlet plate and on the press top and / or Press lower part are hinged, and that the articulation of the Differential cylinder on the upper and / or lower Inlet plate with thermal insulation is made.
- the gimbals Joints of the differential cylinders with interposition supported by insulating material against the inlet plates be in turn, with the interposition of Thermal insulation on frame parts of press top and Press base can support.
- the Hydraulic supply to the differential cylinder under Interposition of a cooling device with a heat exchanger to take place taking into account the heated inlet plates occurring relatively high Temperatures ensure that the differential cylinders work properly to ensure.
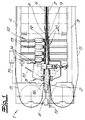
- FIG. 1 there is a continuous press 1 for Pressing pressed material mats 2 to pressed material plates in the train the production of chipboard, fiberboard and others Wood-based panels shown.
- This press instructs Press lower part 3 and an upper press part 4, namely with endless in the lower press part 3 and upper press part 4 circumferential sheet steel press belts 5 and with a Inlet mouth E.
- a heatable press plate 6, 7 is arranged, of which the upper press plate according to the embodiment 6 against the lower press plate 7 for setting the Press nip is adjustable.
- On the press plates 6, 7 close heatable cantilever on the inlet side Inlet plates 8, 9 to form the inlet mouth E.
- the steel sheet press belts 5 are on the press plates 6, 7 and Inlet plates 8, 9 with the interposition of rolling elements 10 or rolling rods supported. Furthermore, a device 11 for adjusting the inlet mouth E and a device 12 for setting the inlet contour of the inlet mouth E intended.
- the device 12 for setting the Inlet contour has a plurality of double-acting Differential cylinders 13 on.
- the differential cylinders 13 are in a predetermined distribution and according to Embodiment on the one hand to the upper inlet plate 8 and on the other hand articulated to the press upper part 4. Further are the differential cylinders 13 to a computer-controlled or regulated hydraulic system 14 connected. Of the Computer 15 and a measuring system 16, which the Mat thickness of the mats to be pressed 2 measures and forwarded to the computer 15 are only indicated.
- the differential cylinders 13 are in longitudinal rows and Cross rows hinged to the upper inlet plate 8. At least this upper inlet plate 8 is drilled lengthways and consequently points in the longitudinal direction of the plate or in the direction of entry extending channels 18 for the heating medium. Due to the longitudinal channels 18 is the upper inlet plate for Absorption of much higher bending stresses than with transverse channels set up.
- the differential cylinders 13 are gimbaled on the upper inlet plate 8 and articulated on the press upper part 4.
- the linkage 19 the differential cylinder 13 on the upper inlet plate a is with the interposition of thermal insulation 20th realized.
- the hydraulic supply to the Differential cylinder 13 with the interposition of one Cooling device done with a heat exchanger, which is not is shown.
- the lower inlet plate 9 is below Interposition of thermal insulation 20 in the lower press part 3 supported.
- the mouth has E a trumpet-like inlet contour for the Pressing of relatively thick pressed material mats 2.
- 2 is one of the pressing zone 21 upstream Clamping zone 22 realized. After that form the top one Inlet plate 8 and the lower inlet plate 9 in almost Parallel position an inlet contour with an inlet of only low taper for relatively thin pressed material mats 2a.
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Wood Science & Technology (AREA)
- Forests & Forestry (AREA)
- Dry Formation Of Fiberboard And The Like (AREA)
- Press Drives And Press Lines (AREA)
- Veneer Processing And Manufacture Of Plywood (AREA)
- Control Of Presses (AREA)
- Inking, Control Or Cleaning Of Printing Machines (AREA)
- Treatment Of Fiber Materials (AREA)
- Press-Shaping Or Shaping Using Conveyers (AREA)
Applications Claiming Priority (6)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE19740325 | 1997-09-13 | ||
| DE19740325A DE19740325C5 (de) | 1997-09-13 | 1997-09-13 | Kontinuierliche Presse zum Verpressen von Preßgutmatten zu Preßgutplatten |
| DE19829742A DE19829742C1 (de) | 1998-07-03 | 1998-07-03 | Kontinuierliche Presse |
| DE19829742 | 1998-07-03 | ||
| DE19829741A DE19829741C1 (de) | 1998-07-03 | 1998-07-03 | Verfahren und Presse zum Verpressen, insbesondere kontinuierlichen Verpressen |
| DE19829741 | 1998-07-03 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0909620A2 true EP0909620A2 (fr) | 1999-04-21 |
| EP0909620A3 EP0909620A3 (fr) | 1999-05-19 |
| EP0909620B1 EP0909620B1 (fr) | 2003-11-19 |
Family
ID=27217743
Family Applications (3)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98117029A Expired - Lifetime EP0901894B1 (fr) | 1997-09-13 | 1998-09-09 | Procédé et presse pour le pressage, en particulier pressage en continu |
| EP98117030A Expired - Lifetime EP0909620B1 (fr) | 1997-09-13 | 1998-09-09 | Presse continue pour le pressage de nattes en panneaux |
| EP03020741A Expired - Lifetime EP1371466B1 (fr) | 1997-09-13 | 1998-09-09 | Presse pour le pressage en continu |
Family Applications Before (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98117029A Expired - Lifetime EP0901894B1 (fr) | 1997-09-13 | 1998-09-09 | Procédé et presse pour le pressage, en particulier pressage en continu |
Family Applications After (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP03020741A Expired - Lifetime EP1371466B1 (fr) | 1997-09-13 | 1998-09-09 | Presse pour le pressage en continu |
Country Status (5)
| Country | Link |
|---|---|
| US (2) | US6098532A (fr) |
| EP (3) | EP0901894B1 (fr) |
| CN (2) | CN1076258C (fr) |
| CA (2) | CA2244283C (fr) |
| DE (2) | DE59810212D1 (fr) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP3858590A1 (fr) * | 2020-01-29 | 2021-08-04 | Siempelkamp Maschinen- und Anlagenbau GmbH | Procédé de surveillance d'une bande d'acier dans une presse continue et presse continue |
Families Citing this family (46)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19918492C5 (de) * | 1999-04-23 | 2006-10-05 | Siempelkamp Maschinen- Und Anlagenbau Gmbh & Co. Kg | Verfahren zum Verpressen von Preßgutmatten zu Preßgutplatten im Zuge der Herstellung von Spanplatten, Faserplatten und anderen Holzwerkstoffplatten |
| ZA200308100B (en) * | 2001-04-18 | 2004-10-18 | Coe Mfg Co | Belt making apparatus and method. |
| CA2352414A1 (fr) * | 2001-07-05 | 2003-01-05 | Industries Fournier Inc. | Dispositif de controle et de retenue des gateaux dans un pressoir rotatif |
| US20030136312A1 (en) * | 2001-11-30 | 2003-07-24 | Nelson Guimil | Configuration applied to a multi-adjustable piece of furniture |
| DE10214322B4 (de) * | 2002-03-28 | 2016-07-14 | Siempelkamp Maschinen- Und Anlagenbau Gmbh | Kontinuierliche Presse zum Verpressen von Pressgutmatten zu Pressgutplatten |
| US7196290B2 (en) * | 2003-06-02 | 2007-03-27 | Planet Products Corporation | Heat sealer with platen surface temperature sensor and load sensor |
| US7449517B1 (en) | 2003-06-21 | 2008-11-11 | James Rock Associates, Llc | Composite building material |
| EP1820304B1 (fr) | 2004-12-03 | 2014-05-07 | Telecom Italia S.p.A. | Autorisation de services combinatoires dans un reseau de communication |
| DE102005009334B4 (de) * | 2005-03-01 | 2016-03-24 | Siempelkamp Maschinen- Und Anlagenbau Gmbh | Kontinuierliche Presse |
| DE102005009298B4 (de) * | 2005-03-01 | 2016-07-07 | Siempelkamp Maschinen- Und Anlagenbau Gmbh | Kontinuierliche Presse |
| DE102005024065B3 (de) * | 2005-05-25 | 2006-09-14 | Siempelkamp Maschinen- Und Anlagenbau Gmbh & Co. Kg | Kontinuierliche Presse |
| CN100377855C (zh) * | 2005-09-27 | 2008-04-02 | 上海人造板机器厂有限公司 | 平压式连续压机中热压板的定位方法及定位板结构 |
| US7354543B2 (en) * | 2005-09-28 | 2008-04-08 | Weyerhaeuser Company | Manufactured wood product press |
| US20070111019A1 (en) * | 2005-11-04 | 2007-05-17 | Ainsworth Lumber Co., Ltd. | Methods of manufacturing engineered wood products |
| US20070102113A1 (en) * | 2005-11-04 | 2007-05-10 | Ainsworth Lumber Co., Ltd. | Methods of manufacturing engineered wood products |
| DE102006059564B4 (de) * | 2006-12-16 | 2009-06-18 | Siempelkamp Maschinen- Und Anlagenbau Gmbh & Co. Kg | Verfahren und Vorrichtung zum Verpressen von Pressgutmatten |
| US20090077924A1 (en) * | 2007-09-21 | 2009-03-26 | Ainsworth Lumber Co., Ltd. | Methods of manufacturing engineered wood products |
| CN102159370B (zh) * | 2008-05-26 | 2014-12-03 | Pbh农业纤维板材公司 | 将颗粒材料粘合到制造物品 |
| WO2009155701A1 (fr) * | 2008-06-27 | 2009-12-30 | Mario Antonio Rago | Presse continue et procédé de fabrication de matériaux composites par pression symétrique progressive |
| CN101508127B (zh) * | 2009-03-23 | 2013-09-25 | 中国福马机械集团有限公司 | 连续压制压制品坯料的连续压机 |
| CN101508128B (zh) * | 2009-03-23 | 2012-04-25 | 中国福马机械集团有限公司 | 利用连续压机压制压制品的方法和用于实施该方法的设备 |
| CN102285139B (zh) * | 2011-06-01 | 2014-07-09 | 上海板机电气制造有限公司 | 一种平板式连续压机的控制装置 |
| CN102259372A (zh) * | 2011-08-05 | 2011-11-30 | 青岛国森机械有限公司 | 一种长规格竹木集成材压制设备 |
| US9458298B2 (en) | 2012-10-01 | 2016-10-04 | Georgia-Pacific Chemicals Llc | Methods for making lignocellulose containing composite products |
| US9586338B2 (en) | 2012-10-01 | 2017-03-07 | Georgia-Pacific Chemicals Llc | Methods for making lignocellulose containing composite products |
| CA2902930C (fr) | 2013-03-14 | 2018-01-23 | Georgia-Pacific Chemicals Llc | Compositions de liant qui comprennent un compose polyphenolique, un compose insature et un precurseur de radical libre, et methode de fabrication et utilisation associee |
| US9193894B2 (en) | 2013-03-14 | 2015-11-24 | Georgia-Pacific Chemicals Llc | Binder compositions and methods for making and using same |
| US9587077B2 (en) | 2013-03-14 | 2017-03-07 | Georgia-Pacific Chemicals Llc | Methods for making composite products containing lignocellulose substrates |
| WO2015153517A1 (fr) | 2014-04-02 | 2015-10-08 | Georgia-Pacific Chemicals Llc | Procédés de fabrication de produits composites lignocellulosiques |
| US9617427B2 (en) | 2014-04-02 | 2017-04-11 | Georgia-Pacific Chemicals Llc | Methods for making lignocellulose composite products with oxidative binders and encapsulated catalyst |
| US9587114B2 (en) | 2014-04-02 | 2017-03-07 | Georgia-Pacific Chemicals Llc | Methods for making lignocellulose composite products with oxidative binders and complexed metal catalyst |
| US10011041B2 (en) | 2015-05-15 | 2018-07-03 | Usnr, Llc | Modular press |
| KR101686968B1 (ko) * | 2015-08-12 | 2016-12-28 | 주식회사 진관 | 단열판재 성형장치 |
| WO2017205698A1 (fr) | 2016-05-26 | 2017-11-30 | Georgia-Pacific Chemicals Llc | Liants contenant une résine à base d'aldéhyde et une résine à base d'isocyanate et procédés de fabrication de produits lignocellulosiques composites à partir de ceux-ci |
| WO2018023095A1 (fr) | 2016-07-29 | 2018-02-01 | Georgia-Pacific Chemicals Llc | Procédés de fabrication de produits composites avec des liants contenant des isocyanates bloqués |
| ES2756337T3 (es) * | 2016-10-06 | 2020-04-27 | SWISS KRONO Tec AG | Equipo de prensa para placas de compuesto de madera y procedimiento para vigilar un equipo de prensa para placas de compuesto de madera |
| US11400676B2 (en) | 2016-10-06 | 2022-08-02 | SWISS KRONO Tec AG | Wood material panel pressing device and method for monitoring a wood material panel pressing device |
| CN107913890B (zh) * | 2016-10-08 | 2024-08-23 | 宁波荣轩新材料有限公司 | 一种环保型垃圾处理设备 |
| IT201600105117A1 (it) * | 2016-10-19 | 2018-04-19 | Sacmi | Macchina per la compattazione di materiale in polvere |
| DE102017110301A1 (de) * | 2017-05-11 | 2018-11-15 | Dieffenbacher GmbH Maschinen- und Anlagenbau | Verfahren zur Überwachung wenigstens einer Komponente eines Rollstangenteppichs einer kontinuierlich arbeitenden Presse, Überwachungsvorrichtung und kontinuierlich arbeitende Presse |
| DE102017110995A1 (de) * | 2017-05-19 | 2018-11-22 | Dieffenbacher GmbH Maschinen- und Anlagenbau | Vorpresse und System zum kontinuierlichen Herstellen von Werkstoffplatten, Verfahren zum Einbringen oder Entnehmen des Pressenbandes und Transportvorrichtung zum Aufnehmen des Pressenbandes |
| EP3793817B1 (fr) * | 2018-05-14 | 2024-11-13 | DIEFFENBACHER GMBH Maschinen- und Anlagenbau | Procédé de surveillance d'au moins un élément d'un tapis roulant à tiges d'une presse fonctionnant en continu, dispositif de surveillance et presse fonctionnant en continu |
| CN108995193A (zh) * | 2018-09-06 | 2018-12-14 | 浙江冠森新材料有限公司 | 一种防止木塑板材变形的模压机 |
| DE102019000767B4 (de) * | 2019-02-02 | 2021-03-25 | Siempelkamp Maschinen- Und Anlagenbau Gmbh | Vorrichtung und Verfahren zur Dämmplattenherstellung |
| US20240009886A1 (en) * | 2019-10-18 | 2024-01-11 | Välinge Innovation AB | Methods and arrangements for continuous manufacture of building panels |
| CN116061288A (zh) * | 2023-02-07 | 2023-05-05 | 亚联机械制造(唐山)有限公司 | 一种用于双钢带连续压制机的钢带跑偏调整方法 |
Family Cites Families (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3942929A (en) * | 1972-03-08 | 1976-03-09 | Bison-Werke Bahre & Greten Gmbh & Co. Kg | Continuously operating press |
| DE3133817C3 (de) * | 1981-08-27 | 1996-02-08 | Siempelkamp Gmbh & Co | Vorrichtung zum kontinuierlichen Pressen von Preßgutmatten |
| DE3734180C2 (de) * | 1987-10-09 | 1998-01-29 | Kuesters Eduard Maschf | Doppelbandpresse zur Herstellung von Holzspanplatten und dergleichen |
| DE4042531C3 (de) * | 1990-10-15 | 2002-02-07 | Dieffenbacher Gmbh Maschf | Kontinuierlich arbeitende Presse |
| DE4301594C2 (de) * | 1993-01-21 | 2002-10-31 | Dieffenbacher Gmbh Maschf | Verfahren und Anlage zur Herstellung von Spanplatten |
| DE4433643C1 (de) * | 1993-12-11 | 1996-02-08 | Siempelkamp Gmbh & Co | Kontinuierliche Presse für die Herstellung von Spanplatten, Faserplatten, Laminatplatten und ähnlichen Preßgutplatten |
| DE4405342B4 (de) * | 1994-02-19 | 2004-05-27 | Maschinenfabrik J. Dieffenbacher Gmbh & Co | Kontinuierlich arbeitende Presse |
| DE4433641C1 (de) * | 1994-09-21 | 1995-11-02 | Siempelkamp Gmbh & Co | Kontinuierliche Presse zum Verpressen von Preßgutmatten zu Preßgutplatten |
| DE4446091A1 (de) * | 1994-12-22 | 1996-06-27 | Dieffenbacher Gmbh Maschf | Pressengestell |
| DE19518879A1 (de) * | 1995-05-28 | 1996-12-05 | Dieffenbacher Gmbh Maschf | Verfahren und Anlage zur Herstellung von Spanplatten |
-
1998
- 1998-09-09 DE DE59810212T patent/DE59810212D1/de not_active Expired - Lifetime
- 1998-09-09 DE DE59812293T patent/DE59812293D1/de not_active Expired - Lifetime
- 1998-09-09 EP EP98117029A patent/EP0901894B1/fr not_active Expired - Lifetime
- 1998-09-09 EP EP98117030A patent/EP0909620B1/fr not_active Expired - Lifetime
- 1998-09-09 EP EP03020741A patent/EP1371466B1/fr not_active Expired - Lifetime
- 1998-09-14 CN CN98124377A patent/CN1076258C/zh not_active Ceased
- 1998-09-14 CN CNB981243762A patent/CN1188259C/zh not_active Expired - Lifetime
- 1998-09-14 CA CA002244283A patent/CA2244283C/fr not_active Expired - Lifetime
- 1998-09-14 CA CA002244284A patent/CA2244284C/fr not_active Expired - Lifetime
- 1998-09-14 US US09/152,941 patent/US6098532A/en not_active Expired - Lifetime
- 1998-09-14 US US09/152,931 patent/US6142068A/en not_active Expired - Lifetime
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP3858590A1 (fr) * | 2020-01-29 | 2021-08-04 | Siempelkamp Maschinen- und Anlagenbau GmbH | Procédé de surveillance d'une bande d'acier dans une presse continue et presse continue |
Also Published As
| Publication number | Publication date |
|---|---|
| US6098532A (en) | 2000-08-08 |
| CN1224650A (zh) | 1999-08-04 |
| CA2244283C (fr) | 2003-07-29 |
| EP0909620B1 (fr) | 2003-11-19 |
| EP0909620A3 (fr) | 1999-05-19 |
| DE59810212D1 (de) | 2003-12-24 |
| CN1224651A (zh) | 1999-08-04 |
| EP0901894B1 (fr) | 2004-11-24 |
| CA2244283A1 (fr) | 1999-03-13 |
| CN1188259C (zh) | 2005-02-09 |
| DE59812293D1 (de) | 2004-12-30 |
| EP0901894A3 (fr) | 1999-05-12 |
| EP1371466B1 (fr) | 2011-06-29 |
| EP1371466A1 (fr) | 2003-12-17 |
| US6142068A (en) | 2000-11-07 |
| CN1076258C (zh) | 2001-12-19 |
| EP0901894A2 (fr) | 1999-03-17 |
| CA2244284C (fr) | 2002-05-28 |
| CA2244284A1 (fr) | 1999-03-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0909620B1 (fr) | Presse continue pour le pressage de nattes en panneaux | |
| DE10214322B4 (de) | Kontinuierliche Presse zum Verpressen von Pressgutmatten zu Pressgutplatten | |
| DE4301594C2 (de) | Verfahren und Anlage zur Herstellung von Spanplatten | |
| EP2089197B1 (fr) | Procédé pour comprimer des nattes de matériau comprimable | |
| DE4340982B4 (de) | Kontinuierlich arbeitende Presse | |
| DE19740325C1 (de) | Kontinuierliche Presse zum Verpressen von Preßgutmatten zu Preßgutplatten | |
| EP0394697A2 (fr) | Installation de pressage pour presser continuellement des matières en forme de bande | |
| DE102008022857A1 (de) | Kontinuierlich arbeitende Presse zur Herstellung von Werkstoffplatten, ein Verfahren zum Betreiben derselben Presse und eine Steuer- und Regelvorrichtung für die kontinuierlich arbeitende Presse | |
| DE4405342A1 (de) | Kontinuierlich arbeitende Presse | |
| EP1825993A2 (fr) | Procédé et presse fonctionnant en continu destinés à la fabrication de plaques de matière première | |
| EP1199152A2 (fr) | Dispositif de réglage de l'espacement de cylindres dans une machine d'encollage de papier ondulé | |
| DE102017110875B4 (de) | Verfahren zum Verpressen einer Pressgutmatte | |
| EP1046483B1 (fr) | Procédé pour le pressage de nattes en panneaux pour la production des panneaux de particules, des panneaux de fibres et autres panneaux lignocellulosiques | |
| DE4340983B4 (de) | Kontinuierlich arbeitende Presse | |
| EP0140117B1 (fr) | Presse à travailler continuellement pour presser un lé de matière en mouvement | |
| DE10045681A1 (de) | Kontinuierlich arbeitende Presse | |
| EP0151422B1 (fr) | Presse à double ruban pour un lé en mouvement continu | |
| DE19806707C2 (de) | Kontinuierliche Presse zum Verpressen von Preßgutmatten zu Preßgutplatten | |
| DE4400347C5 (de) | Kontinuierlich arbeitende Presse | |
| DE19824723C1 (de) | Verfahren und kontinuierliche Presse zum Einstellen der Einlaufkontur des Einlaufmauls der Presse | |
| DE19829742C1 (de) | Kontinuierliche Presse | |
| DE3914107C2 (de) | Kontinuierliche Presse zum Pressen und Wärmebehandeln von Preßgutmatten | |
| EP3403816B1 (fr) | Procédé de compression d'une natte de matériau comprimable | |
| DE102005053920B4 (de) | Verfahren zum Einstellen eines Einlaufkeilverdichters einer kontinuierlich arbeitenden Presse im Zuge der Herstellung von Werkstoffplatten und eine kontinuierlich arbeitende Presse zur Durchführung des Verfahrens | |
| DE19525339C2 (de) | Verfahren zur Herstellung von dreischichtigen Holzwerkstoffplatten, insbesondere von Spanplatten oder Faserplatten |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): DE FI FR GB IT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: GAWLITTA,WERNER Inventor name: SCHUERMANN, KLAUS, DIPL.-ING. Inventor name: SEBASTIAN, LOTHAR, DIPL.-ING. Inventor name: WEISS, HORST |
|
| 17P | Request for examination filed |
Effective date: 19991001 |
|
| AKX | Designation fees paid |
Free format text: DE FI FR GB IT SE |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SIEMPELKAMP MASCHINEN- UND ANLAGENBAU GMBH & C |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FI FR GB IT SE |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| REF | Corresponds to: |
Ref document number: 59810212 Country of ref document: DE Date of ref document: 20031224 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| ET | Fr: translation filed | ||
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PLBQ | Unpublished change to opponent data |
Free format text: ORIGINAL CODE: EPIDOS OPPO |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| 26 | Opposition filed |
Opponent name: DIEFFENBACHER GMBH + CO. KG Effective date: 20040819 Opponent name: METSO PANELBOARD GMBHPATENTANWAELTE Effective date: 20040729 |
|
| PLAX | Notice of opposition and request to file observation + time limit sent |
Free format text: ORIGINAL CODE: EPIDOSNOBS2 |
|
| PLBB | Reply of patent proprietor to notice(s) of opposition received |
Free format text: ORIGINAL CODE: EPIDOSNOBS3 |
|
| PLBP | Opposition withdrawn |
Free format text: ORIGINAL CODE: 0009264 |
|
| PLCK | Communication despatched that opposition was rejected |
Free format text: ORIGINAL CODE: EPIDOSNREJ1 |
|
| PLBN | Opposition rejected |
Free format text: ORIGINAL CODE: 0009273 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: OPPOSITION REJECTED |
|
| 27O | Opposition rejected |
Effective date: 20090202 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 59810212 Country of ref document: DE Representative=s name: ANDREJEWSKI - HONKE PATENT- UND RECHTSANWAELTE, DE |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 59810212 Country of ref document: DE Representative=s name: ANDREJEWSKI - HONKE PATENT- UND RECHTSANWAELTE, DE Effective date: 20141202 Ref country code: DE Ref legal event code: R081 Ref document number: 59810212 Country of ref document: DE Owner name: SIEMPELKAMP MASCHINEN- UND ANLAGENBAU GMBH, DE Free format text: FORMER OWNER: SIEMPELKAMP MASCHINEN- UND ANLAGENBAU GMBH & CO. KG, 47803 KREFELD, DE Effective date: 20141202 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 19 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20170921 Year of fee payment: 20 Ref country code: FR Payment date: 20170920 Year of fee payment: 20 Ref country code: IT Payment date: 20170929 Year of fee payment: 20 Ref country code: FI Payment date: 20170926 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20170921 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20170928 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 59810212 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20180908 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20180908 |