EP0920983A1 - Coussinet pour presse - Google Patents
Coussinet pour presse Download PDFInfo
- Publication number
- EP0920983A1 EP0920983A1 EP98120719A EP98120719A EP0920983A1 EP 0920983 A1 EP0920983 A1 EP 0920983A1 EP 98120719 A EP98120719 A EP 98120719A EP 98120719 A EP98120719 A EP 98120719A EP 0920983 A1 EP0920983 A1 EP 0920983A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- threads
- group
- press pad
- pad according
- press
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 239000013013 elastic material Substances 0.000 claims abstract description 18
- 230000006835 compression Effects 0.000 claims abstract description 7
- 238000007906 compression Methods 0.000 claims abstract description 7
- 239000002184 metal Substances 0.000 claims description 46
- 229910052751 metal Inorganic materials 0.000 claims description 46
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 claims description 16
- 229910052802 copper Inorganic materials 0.000 claims description 16
- 239000010949 copper Substances 0.000 claims description 16
- 239000004033 plastic Substances 0.000 claims description 10
- 229920003023 plastic Polymers 0.000 claims description 10
- 239000004744 fabric Substances 0.000 claims description 8
- 229920002379 silicone rubber Polymers 0.000 claims description 7
- 229920003235 aromatic polyamide Polymers 0.000 claims description 6
- 239000004760 aramid Substances 0.000 claims description 5
- 238000010030 laminating Methods 0.000 claims description 4
- 229910000881 Cu alloy Inorganic materials 0.000 claims description 2
- 239000004696 Poly ether ether ketone Substances 0.000 claims description 2
- JUPQTSLXMOCDHR-UHFFFAOYSA-N benzene-1,4-diol;bis(4-fluorophenyl)methanone Chemical compound OC1=CC=C(O)C=C1.C1=CC(F)=CC=C1C(=O)C1=CC=C(F)C=C1 JUPQTSLXMOCDHR-UHFFFAOYSA-N 0.000 claims description 2
- 150000001879 copper Chemical class 0.000 claims description 2
- 229920001643 poly(ether ketone) Polymers 0.000 claims description 2
- 229920002530 polyetherether ketone Polymers 0.000 claims description 2
- 229920000069 polyphenylene sulfide Polymers 0.000 claims description 2
- 239000003779 heat-resistant material Substances 0.000 claims 1
- 238000009827 uniform distribution Methods 0.000 claims 1
- 239000000463 material Substances 0.000 abstract description 17
- 229920001971 elastomer Polymers 0.000 abstract description 14
- 239000000806 elastomer Substances 0.000 description 10
- 238000000576 coating method Methods 0.000 description 2
- 238000009826 distribution Methods 0.000 description 2
- 239000003365 glass fiber Substances 0.000 description 2
- 238000010438 heat treatment Methods 0.000 description 2
- 230000010354 integration Effects 0.000 description 2
- 239000010410 layer Substances 0.000 description 2
- 239000007769 metal material Substances 0.000 description 2
- 229910001369 Brass Inorganic materials 0.000 description 1
- 238000005299 abrasion Methods 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000010951 brass Substances 0.000 description 1
- 239000011093 chipboard Substances 0.000 description 1
- 238000005253 cladding Methods 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 238000005265 energy consumption Methods 0.000 description 1
- 230000002349 favourable effect Effects 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 239000002356 single layer Substances 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
- 238000004804 winding Methods 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B15/00—Details of, or accessories for, presses; Auxiliary measures in connection with pressing
- B30B15/06—Platens or press rams
- B30B15/061—Cushion plates
Definitions
- the invention relates to a press pad for use in Laminating presses with a fabric that is a first group parallel threads and a second group of parallel ones Has threads of the first group of crossing threads, wherein the threads of the first group consist of metal or one Have metal content and the threads of the second Group consist of rubber-elastic material or one Share of it, and being the threads of the first group to pull the threads of the second group.
- layer materials for example decorative chipboard coatings
- laminating presses which as low or high pressure floor presses or short-cycle presses
- Press pads used to do the job Full pressure on the material to be pressed evenly transfer.
- the press pads need high pressures as well withstand the temperatures in such presses can, and they must be able to respond to those of the Press plates outgoing heat quickly and without major losses to transfer to the pressed material, so a high thermal conductivity to have in this direction.
- Press pads are known in the prior art, which are made of a fabric consisting of two types of threads (EP 0 493 630 A1).
- Threads made of metal or have a metal component around which To improve heat transfer to the pressed material.
- Threads made of aromatic polyamide EP 0 493 630 A1
- silicone elastomer DE 295 18 204 U1
- rubber heat-resistant plastic monofilament or the like
- the invention thus lies in based primarily on the task of using a press pad to create better thermal conductivity. Another The task is to improve dimensional stability and to provide a smooth surface.
- the thread density of the threads of the second group is so great that the threads of the first group are only under compression the elastic material of the threads of the second Group go through between them.
- Basic idea It is therefore the invention, through a special fabric geometry with a very high thread density in the threads of the second group has a positive influence on heat transfer to take.
- the threads are woven so that the threads of the first group not about the outermost points of the threads of the second group formed level, better still Distance from this level.
- This training has the Advantage that the threads of the first group when handling the press pad are protected against abrasion. First in case of pressure in the laminating press they get Threads of the first group (metal threads) contact the adjacent ones Surfaces of the press and the material to be pressed and care then for good heat conduction.
- that the thread density of the threads of the first group is so high is that the area coverage is between 50 and 80%, preferably is between 60 and 70%. This high thread density also promotes thermal conductivity and thus the rapid heating of the pressed material.
- the threads have a weave with an even distribution of the cranks of the threads of the first group.
- the number of cranks of the threads of the first group should be between 20 and 30 per cm 2 on each side of the fabric. This high density of the cranks also ensures good heat transfer that is uniform over the surface.
- the rubber-elastic material has a Shore A hardness of Has 60 to 75. This hardness favors the storage of Threads of the first group and thus a firm tissue bond. In addition, the remaining compressibility remains with this Preserve hardness for a long time.
- All materials that have rubber-elastic properties and are able to withstand the temperatures in the presses are suitable for the rubber-elastic material. Silicone elastomers are particularly suitable. A foamed rubber-elastic material is recommended, preferably with a specific weight of 0.3 to 0.5 g / cm 3 .
- Such metal materials should be used for the threads of the first group be used, which have high thermal conductivity to have. As already mentioned above, this is possible especially copper or strength-modified copper alloys on. Because of the firm tissue integration the tendency of copper threads to shrink is counteracted, so that despite the use of this problematic No significant shrinkage found could be. In this way, the high Thermal conductivity and the low price of this material can be used for the press pad according to the invention.
- the use of is not particularly advantageous annealed copper (hard copper) because it has high strength Has. But also annealed copper (soft copper) comes in question.
- threads of the first group have a plastic core thread have, which is surrounded by at least one metal wire is, preferably in such a way that the Plastic core thread from the metal wire or wires is completely covered.
- the coverage happens preferably by wrapping at least one metal wire, expediently a plurality of metal wires one above the other, or by stranding metal wires.
- Through the Stranding or wrapping of the metal wire or wires occurs in contrast to twisting an almost circular one Thread, which creates a larger contact area Forms top and bottom of the press pad and thus good heat transfer from the press plates to the material to be pressed is achieved.
- the plastic core thread heat-resistant plastics for example aramids, or Monofilaments made of PPS, PEK, PEEK or the like or glass fiber threads in question.
- the invention further provides that threads of the second Group surrounded on the outside with at least one metal wire are, and here preferably so that the threads the second group completely with the outside or the metal wires are covered.
- This has the advantage that the threads of the second group also transfer heat promote, but their cushioning properties not because of the proportion of rubber-elastic material to lose.
- the threads of the second group are wrapped here too, preferably by twisting or wrapping.
- Inside the enclosure through the metal wires the threads of the second group can be made entirely of rubber elastic Material, for example a silicone elastomer consist. Better strength, however reached when these threads have a soul thread, that of an extruded shell made of rubber-elastic Material is surrounded. Thereby the soul thread a central thread, e.g. made of aramid, glass fibers, metal etc., have stranded or wound around the metal wires are.
- the stranded metal wires should be partially S-shaped and partially Z-shaped, this advantageously being done alternately. This can be a Hiking "of the press pad in the press can be avoided effectively.
- the threads of the second group should get one Diameter of at least 1 mm, preferably at least Have 1.5 mm. They then remain within the tissue essentially stretched out, and promote along with their in relation to the thickness of the threads of the first group high thread density a pronounced cranking of these threads.
- the threads of the first group should have a diameter of at least 0.15mm that go to 0.3mm can.
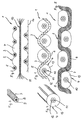
- the press pad 1 shown in Figures 1 and 2 is as a single-layer fabric 2 with extending in the warp direction Longitudinal threads - labeled 3 by way of example - and transverse threads extending in the weft direction - exemplary designated with 4 - trained.
- the run Cross threads 4 essentially stretched, i.e. you will be not essential due to the integration with the longitudinal threads 3 pressed out of the press pad level while lay the longitudinal threads 3 around the transverse threads 4 and pronounced cranking on the top and bottom - exemplified with 5, 6 form, which are in Flatten operation under pressure and the between the transverse threads 4 through intermediate sections - for example designated 7 - are connected. This way there is a meandering course of the longitudinal threads 3.
- a longitudinal thread 3 is shown in more detail in FIG. It has a twisted soul thread 8 made of aramid on the six metal wires - exemplary with 9 designated - are beaten according to the type of stranding, and in such a way that the soul thread 8 completely from the Metal wires 9 is wrapped. This results in a very closed and relatively smooth surface of the Longitudinal thread 3, which ensures good contact with the Press plates and to the material to be pressed.
- the longitudinal thread 3 has a diameter of 0.2 mm.
- the cross thread 4 shown enlarged in FIG. 4 has a soul thread 10 of 0.2 mm in diameter, which from a Central thread 11 made of aramid and six metal wires - designated by way of example with 12 - consists of the metal wires 12 are stranded around the central thread 11. Of the Metal wire 12 is made of non-annealed copper (Copper hard), which achieves high strength becomes.
- the soul thread 10 is of an extruded on Elastomer sleeve 13 surrounded by a silicone elastomer. This results in a diameter for the transverse threads 4 of 1.5 mm.
- the thread density is Cross threads 4 dimensioned so that the distance of the cross threads 4th without longitudinal threads 3 woven in, that is to say in the undeformed state is less than their diameter, i.e. less than 0.2 mm.
- the longitudinal threads 3 thus dig into that elastic material of the elastomer sheath 13 of the transverse threads 4 on. This not only has the advantage that the longitudinal threads 3 not in the direction of the longitudinal axes of the transverse threads 4 can shift, but force the longitudinal threads 3 to Formation of steep intermediate sections 7.
- the deformation of the press pad 1 under compression pressure can refer to Figure 5. It can be seen that the cranks 5, 6 of the longitudinal threads 3 are flattened so that result in elongated heat transfer surfaces. The intermediate sections 7 are deformed so that they are almost vertical run between the transverse threads 4, so that short heat transfer distances from one to the other Side of the press pad 1 result. Both ensure one rapid transfer of heat from the heating plates to the pressed material.
- FIG. 6 shows a cross thread 15 for a thread not shown here shown press pad.
- the cross thread 15 is suitable also in the press pad 1 according to Figures 1 and 2 application to find. It has an elastomer core 16 made of one Silicon elastomer, which - which is not shown here is - surrounds a soul thread that is in the same Is constructed in the same way as for the transverse thread 4.
- Metal wires around the elastomer core 16 are exemplary marked with 17 - stranded. After completing the stranding process is the elastomer core 16 over the entire surface of surrounded by the metal wires 17, making it a complete Form metal cladding.
- the cross thread 15 is therefore for Improvement of the heat transfer through a manufactured with it Suitable press pad, be it as the only metal thread, be it in addition to metal longitudinal threads, be it that the longitudinal threads are formed in the same way like the cross threads 15.
- Figure 7 shows a transverse thread 18, which is a replacement for or in combination with the transverse thread 15 according to FIG. 6 in one Press pad can be used. He also has an elastomer core 19 made of a silicone elastomer, which - what is not shown here - a soul thread surrounds, which is constructed in the same way as that Cross thread 4.
- a metal wire 20 is wound around the elastomer core 19, in such a way that it covers the entire area of the elastomer core 19 surrounds and thus a gapless metal coating is formed. It is appropriate that the metal wire 20th of another metal wire in the reverse winding direction is surrounded, so that there is then a two-layer metal covering results. This ensures that even in Bends a complete wrap around the elastomer core 19 is guaranteed.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Woven Fabrics (AREA)
- Mechanical Treatment Of Semiconductor (AREA)
- Liquid Crystal (AREA)
- Laminated Bodies (AREA)
- Bipolar Transistors (AREA)
- Confectionery (AREA)
- Encapsulation Of And Coatings For Semiconductor Or Solid State Devices (AREA)
- Apparatuses For Bulk Treatment Of Fruits And Vegetables And Apparatuses For Preparing Feeds (AREA)
- Surface Heating Bodies (AREA)
- Printing Plates And Materials Therefor (AREA)
- Braking Systems And Boosters (AREA)
- Presses And Accessory Devices Thereof (AREA)
- Magnetically Actuated Valves (AREA)
- Polishing Bodies And Polishing Tools (AREA)
- Finger-Pressure Massage (AREA)
- Absorbent Articles And Supports Therefor (AREA)
- Building Environments (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE29721495U | 1997-12-05 | ||
| DE29721495U DE29721495U1 (de) | 1997-12-05 | 1997-12-05 | Preßpolster |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0920983A1 true EP0920983A1 (fr) | 1999-06-09 |
| EP0920983B1 EP0920983B1 (fr) | 2003-09-10 |
Family
ID=8049522
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98120719A Expired - Lifetime EP0920983B1 (fr) | 1997-12-05 | 1998-10-31 | Coussinet pour presse |
Country Status (10)
| Country | Link |
|---|---|
| EP (1) | EP0920983B1 (fr) |
| AT (1) | ATE249334T1 (fr) |
| CZ (1) | CZ294633B6 (fr) |
| DE (2) | DE29721495U1 (fr) |
| DK (1) | DK0920983T3 (fr) |
| ES (1) | ES2203869T3 (fr) |
| HU (1) | HU219898B (fr) |
| PL (1) | PL188168B1 (fr) |
| PT (1) | PT920983E (fr) |
| SK (1) | SK284583B6 (fr) |
Cited By (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2001076861A1 (fr) * | 2000-04-08 | 2001-10-18 | Marathon Belting Limited | Coussinets de pression |
| US6342457B1 (en) | 1999-03-03 | 2002-01-29 | Thomas Josef Heimbach Gesellschaft Mit Beschrankter Haftung & Co. | Pressing cushion |
| WO2002026480A1 (fr) * | 2000-09-26 | 2002-04-04 | Marathon Belting Limited | Tampon de presse |
| US6413889B1 (en) | 1999-03-03 | 2002-07-02 | Thomas Josef Heimbach Gesellschaft Mit Beschrankter Haftung & Co. | Pressing cushion |
| EP1300235A1 (fr) * | 2001-09-27 | 2003-04-09 | Thomas Josef Heimbach Gesellschaft mit beschränkter Haftung & Co. | Coussinet pour presse |
| EP1386723A3 (fr) * | 2002-07-31 | 2004-06-02 | RHEINISCHE FILZTUCHFABRIK GmbH | Coussinet pour presse |
| US6780280B2 (en) | 2001-09-27 | 2004-08-24 | Thomas Josef Heimbach Gesellschaft Mit Beschrankter Haftung & Co. | Pressing cushion |
| EP1508433A1 (fr) * | 2003-08-13 | 2005-02-23 | RHEINISCHE FILZTUCHFABRIK GmbH | Coussinet de presse |
| WO2007129041A1 (fr) | 2006-05-03 | 2007-11-15 | Marathon Belting Limited | amÉliorations apportÉes aux patins de presse |
| DE202010001226U1 (de) | 2010-01-20 | 2011-05-26 | Helmbach GmbH & Co. KG, 52353 | Presspolster |
| CN1966794B (zh) * | 2005-10-28 | 2012-02-15 | 莱茵里希毛毡工厂有限责任公司 | 用于液压热压设备的压力平衡织物 |
| EP2664450A3 (fr) * | 2012-05-16 | 2016-06-01 | Hueck Rheinische GmbH | Coussin de presse ainsi que fils d'élastomère résistant aux températures élevées |
| WO2024141250A1 (fr) | 2022-12-30 | 2024-07-04 | Hueck Rheinische Gmbh | Coussin de presse comprenant un tissu et presse à chaud |
Families Citing this family (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1040909B1 (fr) * | 1999-03-03 | 2001-08-08 | Thomas Josef Heimbach Gesellschaft mit beschränkter Haftung & Co. | Coussinet pour presse |
| DE20005266U1 (de) * | 2000-03-22 | 2001-05-10 | R. Bruch & Cie. S.A., Neu-Moresnet | Presspolster sowie Heizplattenpresse mit solchen Presspolstern |
| DE10124090B4 (de) * | 2001-02-02 | 2012-07-12 | Gkd - Gebr. Kufferath Ag | Produktionsmaschine für verdichtete Holzprodukte sowie Verwendung eines Mischgewebes für derarige Produktionsmaschinen |
| DE102007013871A1 (de) * | 2007-03-20 | 2008-09-25 | Gkd - Gebr. Kufferath Ag | Aufgerauter Schussdraht |
| DE202007006849U1 (de) | 2007-05-10 | 2008-06-26 | Heimbach Gmbh & Co. Kg | Presspolster mit Randverstärkung |
| DE202016000367U1 (de) * | 2016-01-20 | 2016-02-05 | Rolf Espe | Presspolster für Ein- und Mehretagenpressen deren Polsterschicht aus Silikonelastomer im 3D-Druckverfahren aufgetragen wird. |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2239340A1 (en) * | 1973-07-31 | 1975-02-28 | Becker & Van Huellen | Press for wood-based materials - with integral lower support of glass fibre for wet or dry pressing |
| JPS61194237A (ja) * | 1985-02-21 | 1986-08-28 | 東レ・デュポン株式会社 | 金属線複合弾性糸 |
| US5298322A (en) * | 1990-12-31 | 1994-03-29 | Rheinische Filztuchfabrik Gmbh | Press pad for high-pressure presses |
| DE29518204U1 (de) * | 1994-10-26 | 1996-05-09 | Marathon Belting Ltd., Rochdale | Preßpolster für eine Schichtstoffpresse |
| EP0713762A2 (fr) * | 1994-11-25 | 1996-05-29 | RHEINISCHE FILZTUCHFABRIK GmbH | Coussinet de pressage pour presses à haute et à basse pression |
| DE29704258U1 (de) * | 1997-03-08 | 1997-06-05 | Rheinische Filztuchfabrik GmbH, 52222 Stolberg | Druckausgleichspolster für Heiz- und Rückkühlpressen |
-
1997
- 1997-12-05 DE DE29721495U patent/DE29721495U1/de not_active Expired - Lifetime
-
1998
- 1998-10-31 DK DK98120719T patent/DK0920983T3/da active
- 1998-10-31 EP EP98120719A patent/EP0920983B1/fr not_active Expired - Lifetime
- 1998-10-31 DE DE59809559T patent/DE59809559D1/de not_active Expired - Lifetime
- 1998-10-31 AT AT98120719T patent/ATE249334T1/de active
- 1998-10-31 ES ES98120719T patent/ES2203869T3/es not_active Expired - Lifetime
- 1998-10-31 PT PT98120719T patent/PT920983E/pt unknown
- 1998-11-24 CZ CZ19983821A patent/CZ294633B6/cs not_active IP Right Cessation
- 1998-11-30 HU HU9802776A patent/HU219898B/hu not_active IP Right Cessation
- 1998-12-04 PL PL98330109A patent/PL188168B1/pl not_active IP Right Cessation
- 1998-12-04 SK SK1668-98A patent/SK284583B6/sk not_active IP Right Cessation
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR2239340A1 (en) * | 1973-07-31 | 1975-02-28 | Becker & Van Huellen | Press for wood-based materials - with integral lower support of glass fibre for wet or dry pressing |
| JPS61194237A (ja) * | 1985-02-21 | 1986-08-28 | 東レ・デュポン株式会社 | 金属線複合弾性糸 |
| US5298322A (en) * | 1990-12-31 | 1994-03-29 | Rheinische Filztuchfabrik Gmbh | Press pad for high-pressure presses |
| DE29518204U1 (de) * | 1994-10-26 | 1996-05-09 | Marathon Belting Ltd., Rochdale | Preßpolster für eine Schichtstoffpresse |
| EP0713762A2 (fr) * | 1994-11-25 | 1996-05-29 | RHEINISCHE FILZTUCHFABRIK GmbH | Coussinet de pressage pour presses à haute et à basse pression |
| DE29704258U1 (de) * | 1997-03-08 | 1997-06-05 | Rheinische Filztuchfabrik GmbH, 52222 Stolberg | Druckausgleichspolster für Heiz- und Rückkühlpressen |
Non-Patent Citations (1)
| Title |
|---|
| DATABASE WPI Section Ch Week 8641, Derwent World Patents Index; Class F02, AN 86-268011, XP002098255 * |
Cited By (20)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6342457B1 (en) | 1999-03-03 | 2002-01-29 | Thomas Josef Heimbach Gesellschaft Mit Beschrankter Haftung & Co. | Pressing cushion |
| US6413889B1 (en) | 1999-03-03 | 2002-07-02 | Thomas Josef Heimbach Gesellschaft Mit Beschrankter Haftung & Co. | Pressing cushion |
| WO2001076861A1 (fr) * | 2000-04-08 | 2001-10-18 | Marathon Belting Limited | Coussinets de pression |
| WO2002026480A1 (fr) * | 2000-09-26 | 2002-04-04 | Marathon Belting Limited | Tampon de presse |
| CN100439089C (zh) * | 2001-09-27 | 2008-12-03 | 托马斯约瑟夫亨巴赫有限公司 | 压垫 |
| EP1300235A1 (fr) * | 2001-09-27 | 2003-04-09 | Thomas Josef Heimbach Gesellschaft mit beschränkter Haftung & Co. | Coussinet pour presse |
| US6780280B2 (en) | 2001-09-27 | 2004-08-24 | Thomas Josef Heimbach Gesellschaft Mit Beschrankter Haftung & Co. | Pressing cushion |
| CZ296958B6 (cs) * | 2001-09-27 | 2006-08-16 | Thomas Josef Heimbach Gesellschaft mit beschränkter Haftung & Co. | Lisovací polstár |
| EP1386723A3 (fr) * | 2002-07-31 | 2004-06-02 | RHEINISCHE FILZTUCHFABRIK GmbH | Coussinet pour presse |
| EP1508433A1 (fr) * | 2003-08-13 | 2005-02-23 | RHEINISCHE FILZTUCHFABRIK GmbH | Coussinet de presse |
| CN1966794B (zh) * | 2005-10-28 | 2012-02-15 | 莱茵里希毛毡工厂有限责任公司 | 用于液压热压设备的压力平衡织物 |
| GB2447837A (en) * | 2006-05-03 | 2008-09-24 | Marathon Belting Ltd | Improvements to press pads |
| US7892990B2 (en) | 2006-05-03 | 2011-02-22 | Marathon Belting Limited | Press pads |
| GB2447837B (en) * | 2006-05-03 | 2011-07-13 | Marathon Belting Ltd | Improvements to press pads |
| WO2007129041A1 (fr) | 2006-05-03 | 2007-11-15 | Marathon Belting Limited | amÉliorations apportÉes aux patins de presse |
| CN101432130B (zh) * | 2006-05-03 | 2013-10-16 | 马拉松包带有限公司 | 压力垫的改进 |
| DE202010001226U1 (de) | 2010-01-20 | 2011-05-26 | Helmbach GmbH & Co. KG, 52353 | Presspolster |
| EP2347894A2 (fr) | 2010-01-20 | 2011-07-27 | Heimbach GmbH & Co. KG | Coussinet pour presse |
| EP2664450A3 (fr) * | 2012-05-16 | 2016-06-01 | Hueck Rheinische GmbH | Coussin de presse ainsi que fils d'élastomère résistant aux températures élevées |
| WO2024141250A1 (fr) | 2022-12-30 | 2024-07-04 | Hueck Rheinische Gmbh | Coussin de presse comprenant un tissu et presse à chaud |
Also Published As
| Publication number | Publication date |
|---|---|
| PL330109A1 (en) | 1999-06-07 |
| HU219898B (hu) | 2001-08-28 |
| DE59809559D1 (de) | 2003-10-16 |
| EP0920983B1 (fr) | 2003-09-10 |
| CZ382198A3 (cs) | 1999-06-16 |
| CZ294633B6 (cs) | 2005-02-16 |
| PT920983E (pt) | 2004-01-30 |
| HU9802776D0 (en) | 1999-01-28 |
| DK0920983T3 (da) | 2004-01-26 |
| DE29721495U1 (de) | 1998-02-19 |
| SK284583B6 (sk) | 2005-07-01 |
| PL188168B1 (pl) | 2004-12-31 |
| HUP9802776A1 (hu) | 1999-07-28 |
| ES2203869T3 (es) | 2004-04-16 |
| ATE249334T1 (de) | 2003-09-15 |
| SK166898A3 (en) | 1999-07-12 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0920983B1 (fr) | Coussinet pour presse | |
| EP0609664B1 (fr) | Toile de séchage et son procédé de fabrication | |
| DE19632831B4 (de) | Flexibles Rohr für ein Endoskop | |
| DE3149783C2 (de) | Drahtseil | |
| DE803800C (de) | Drahtkabel fuer metallische Einlagen von Luftreifen | |
| DE69710015T2 (de) | Transportband und Verfahren zur Herstellung | |
| DE2607449A1 (de) | Seil und verfahren zu dessen herstellung | |
| DE202007019506U1 (de) | Verbesserungen an Presspolstern | |
| EP0266786B1 (fr) | Tissu en hélices combinées comprenant des hélices doubles | |
| EP1040909B1 (fr) | Coussinet pour presse | |
| EP1033237A1 (fr) | Coussinet pour presse | |
| EP0920982B1 (fr) | Coussinet pour presse | |
| DE2530009A1 (de) | Geflochtenes band mit leitungselementen | |
| EP0701080A2 (fr) | Tuyau flexible sous pression résistant à la chaleur | |
| DE3930315A1 (de) | Gewebeband zur verwendung in der pressenpartie einer papiermaschine | |
| EP1063081A2 (fr) | Profilé, son utilisation et procédé pour le fabriquer | |
| EP2347894B1 (fr) | Coussinet pour presse | |
| DE3402620A1 (de) | Drahtgliederband | |
| DE2842296A1 (de) | Verstaerkungsmaterial und -verfahren fuer federnde gegenstaende | |
| DE2822693A1 (de) | Seil aus metalldraehten zum verstaerken von plast- und elastartikeln und verfahren und vorrichtung zu seiner herstellung | |
| DE2339941C3 (de) | Förderband für einen Zugseil-Gurtbandförderer | |
| DE20001177U1 (de) | Preßpolster | |
| DE3215986A1 (de) | Dehnungsschnur | |
| EP1485248B1 (fr) | Tissu textile de verre/ptfe | |
| WO1993024689A1 (fr) | Fils en fibres textiles torsades avec un fil metallique, et leur procede de production |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LI LU NL PT |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 19990611 |
|
| AKX | Designation fees paid |
Free format text: AT BE CH DE DK ES FI FR GB GR IE IT LI LU NL PT |
|
| 17Q | First examination report despatched |
Effective date: 20020628 |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LI LU NL PT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030910 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REF | Corresponds to: |
Ref document number: 59809559 Country of ref document: DE Date of ref document: 20031016 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: GERMAN |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: EP Ref document number: 20030404014 Country of ref document: GR |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20031112 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2203869 Country of ref document: ES Kind code of ref document: T3 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20040614 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 20091026 Year of fee payment: 12 Ref country code: IE Payment date: 20091021 Year of fee payment: 12 Ref country code: ES Payment date: 20091026 Year of fee payment: 12 Ref country code: DK Payment date: 20091023 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20091027 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20091023 Year of fee payment: 12 Ref country code: GB Payment date: 20091023 Year of fee payment: 12 Ref country code: FR Payment date: 20091110 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GR Payment date: 20091022 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PT Payment date: 20101018 Year of fee payment: 13 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V1 Effective date: 20110501 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20101031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101102 Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110503 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20110630 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101031 Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110501 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101031 Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101031 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20111118 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101101 |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: MM4A Free format text: LAPSE DUE TO NON-PAYMENT OF FEES Effective date: 20120430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101031 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20151002 Year of fee payment: 18 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20161031 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20161031 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20170926 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20171023 Year of fee payment: 20 Ref country code: AT Payment date: 20171006 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 59809559 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK07 Ref document number: 249334 Country of ref document: AT Kind code of ref document: T Effective date: 20181031 |