EP0943569B1 - Bobineuse - Google Patents
Bobineuse Download PDFInfo
- Publication number
- EP0943569B1 EP0943569B1 EP99104106A EP99104106A EP0943569B1 EP 0943569 B1 EP0943569 B1 EP 0943569B1 EP 99104106 A EP99104106 A EP 99104106A EP 99104106 A EP99104106 A EP 99104106A EP 0943569 B1 EP0943569 B1 EP 0943569B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- reeling
- reel
- lifting
- drum
- rails
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000011144 upstream manufacturing Methods 0.000 claims abstract description 15
- 239000006096 absorbing agent Substances 0.000 claims description 14
- 230000035939 shock Effects 0.000 claims description 12
- 238000004519 manufacturing process Methods 0.000 claims description 6
- 230000004913 activation Effects 0.000 claims description 5
- 230000001154 acute effect Effects 0.000 claims description 2
- 238000013016 damping Methods 0.000 claims description 2
- 230000007704 transition Effects 0.000 claims description 2
- 238000004804 winding Methods 0.000 description 17
- 230000000903 blocking effect Effects 0.000 description 6
- 238000005096 rolling process Methods 0.000 description 6
- 230000002093 peripheral effect Effects 0.000 description 5
- 230000008878 coupling Effects 0.000 description 3
- 238000010168 coupling process Methods 0.000 description 3
- 238000005859 coupling reaction Methods 0.000 description 3
- 238000005520 cutting process Methods 0.000 description 2
- 238000000034 method Methods 0.000 description 2
- 230000008569 process Effects 0.000 description 2
- 230000001360 synchronised effect Effects 0.000 description 2
- 230000003213 activating effect Effects 0.000 description 1
- 238000013459 approach Methods 0.000 description 1
- 238000006243 chemical reaction Methods 0.000 description 1
- 238000010924 continuous production Methods 0.000 description 1
- 238000006073 displacement reaction Methods 0.000 description 1
- 239000003292 glue Substances 0.000 description 1
- 238000003780 insertion Methods 0.000 description 1
- 230000037431 insertion Effects 0.000 description 1
- 238000012432 intermediate storage Methods 0.000 description 1
- 230000007246 mechanism Effects 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 230000000717 retained effect Effects 0.000 description 1
- 238000007789 sealing Methods 0.000 description 1
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H19/00—Changing the web roll
- B65H19/22—Changing the web roll in winding mechanisms or in connection with winding operations
- B65H19/2238—The web roll being driven by a winding mechanism of the nip or tangential drive type
- B65H19/2253—The web roll being driven by a winding mechanism of the nip or tangential drive type and the roll being displaced during the winding operation
- B65H19/2261—Pope-roller
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H19/00—Changing the web roll
- B65H19/10—Changing the web roll in unwinding mechanisms or in connection with unwinding operations
- B65H19/12—Lifting, transporting, or inserting the web roll; Removing empty core
- B65H19/126—Lifting, transporting, or inserting the web roll; Removing empty core with both-ends supporting arrangements
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H19/00—Changing the web roll
- B65H19/22—Changing the web roll in winding mechanisms or in connection with winding operations
- B65H19/2292—Removing cores or mandrels from web roll after winding
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H19/00—Changing the web roll
- B65H19/22—Changing the web roll in winding mechanisms or in connection with winding operations
- B65H19/30—Lifting, transporting, or removing the web roll; Inserting core
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/40—Type of handling process
- B65H2301/41—Winding, unwinding
- B65H2301/414—Winding
- B65H2301/4148—Winding slitting
- B65H2301/4149—Winding slitting features concerning supply of cores
- B65H2301/41496—Winding slitting features concerning supply of cores loading pre-arranged set of cores
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/40—Type of handling process
- B65H2301/41—Winding, unwinding
- B65H2301/417—Handling or changing web rolls
- B65H2301/4171—Handling web roll
- B65H2301/4172—Handling web roll by circumferential portion, e.g. rolling on circumference
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/40—Type of handling process
- B65H2301/41—Winding, unwinding
- B65H2301/417—Handling or changing web rolls
- B65H2301/4171—Handling web roll
- B65H2301/4173—Handling web roll by central portion, e.g. gripping central portion
- B65H2301/41734—Handling web roll by central portion, e.g. gripping central portion involving rail
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/40—Type of handling process
- B65H2301/41—Winding, unwinding
- B65H2301/417—Handling or changing web rolls
- B65H2301/418—Changing web roll
- B65H2301/4181—Core or mandrel supply
- B65H2301/41816—Core or mandrel supply by core magazine within winding machine, i.e. horizontal or inclined ramp holding cores
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/40—Type of handling process
- B65H2301/41—Winding, unwinding
- B65H2301/417—Handling or changing web rolls
- B65H2301/418—Changing web roll
- B65H2301/4181—Core or mandrel supply
- B65H2301/41818—Core or mandrel supply mandrels circulating (cycling) in machine or system
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2301/00—Handling processes for sheets or webs
- B65H2301/40—Type of handling process
- B65H2301/41—Winding, unwinding
- B65H2301/417—Handling or changing web rolls
- B65H2301/418—Changing web roll
- B65H2301/4182—Core or mandrel insertion, e.g. means for loading core or mandrel in winding position
- B65H2301/41828—Core or mandrel insertion, e.g. means for loading core or mandrel in winding position in axial direction
Definitions
- US-A-4 390 138 describes a reel-up substantially in accordance with the reel-up defined by the preamble of claim 1.
- the lifting device of the known reel-up has lifting elements and actuators. However, the lifting elements are suspended from roller chains and are guided for vertical movement by guideways provided on the inner sides of vertical stands. The lifting elements are thus arranged inside the reel-up for vertical movement between a lower position and upper position by means of cylinders and said roller chains.
- One object of the present invention is therefore to provide an improved reel-up which enables manual handling of the reeling drums to be greatly reduced.
- the reel-up according to the invention is characterized in that
- a surface winding drum 9 is rotatably journalled at the stand parts 6, 7 in the upstream end of the reel-up 1.
- a drive means (not shown) gives the surface winding drum 9 a peripheral speed corresponding to the speed of the paper web 2.
- the stand rails 8 are arranged at a distance from each other which is somewhat greater than the breadth of the paper web 2.
- the reeling drum 4 is provided at each end with a braking drum 10 comprising a coupling member 11 and a bearing housing 12 situated inside the coupling member 11, provided with a peripheral groove 13.
- the reeling drum 4 rolls along the stand parts 6, 7, its peripheral grooves 13 cooperating with the stand rails 8.
- each reeling drum 4 is provided with two form-stable cylindrical cores 14. Alternatively only one core may be used, as shown in Figure 1.
- the reeling drum 4 has expandable plates which in active state, i.e. expanded, lock the cores 14 to the reeling drum and which in inactive state, i.e. unexpanded, release the core from the reel
- the reel-up is provided with a feeding device 22 for feeding a reeling drum 4 along the rails 21 when the reeling drum has been lifted and placed on the rails 21.
- the feeding device 22 comprises a feeder 23 arranged close to each rail 21 to be brought into abutment with a reeling drum when it is to be fed forward.
- the feeding device also comprises a pneumatic actuator 24 arranged on the outer side of each support element 19 to move the feeder 23 to and fro along the rail 21. It will be understood that the two actuators 24 are synchronised with each other.
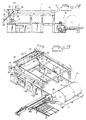
- the reel-up is provided with a pair of lowering arms 32 (see Figures 14 and 15), which are pivotably mounted on the pillars 17 located there. With the aid of these lowering arms 32 a reeling drum 4 is transferred from the exit 29 of the drum stock 15 down to a primary system for receipt of a reeling drum 4 which is arranged in connection with the surface winding drum 9.
- a pair of actuators 34 is arranged at the lowering arms 32, extending between each one lowering arm 32 and the stand part 6, 7, respectively.
- the receiving primary system (see Figures 2-5) comprises two primary arms 38 arranged to receive the new reeling drum 4 either directly from the lowering arms 32 or from a pair of lowering surfaces 39 arranged at each end of the surface winding drum 9 and on a level with its upper side, when the paper reel 3 growing around the reeling drum 4 situated downstream approaches a certain predetermined size (see Figure 6).
- the reel-up 1 further comprises a secondary system having a pair of linearly movable secondary carriages 42 (see Figures 6 and 7) which are displaceable by means of actuators 44 along a track or tracks 45 at each stand part 6, 7.
- the primary arms 38 are arranged to bring the reeling drum 4 into contact with the surface winding drum 9 over which the paper web 2 runs, in order to commence reeling of the paper web 2. While a number of turns of the paper web 2 are wound onto the reeling drum 4, the latter is conveyed by the primary arms 38, along the periphery of the surface winding drum 9 down to the stand parts 6, 7, see Figures 4 and 5, where the secondary system is arranged to take over control of the reeling drum 4 during continued reeling.
- the actuator 44 for the secondary carriage 42 (see Figure 6) consists of a hydraulic or pneumatic cylinder which is secured by one end to the secondary carriage 42 and by its other end to the stand 6, 7.
- the movements of the two secondary carriages 42 along the tracks 45 are thus synchronised with each other and with the increasing diameter of the paper reel 3 so that the secondary carriages 42 follow the paper reel 3 along its horizontal movement during the continued reeling to a finished jumbo roll 3.
- Each primary and secondary system comprises gripping members formed by a locking device 47 and a press device 48.
- the gripping members support the reeling drum 4 while at the same time allowing it to rotate freely inside the gripping members.
- the gripping members of the secondary system is arranged to receive the reeling drum 4 from the gripping members of the primary system so that the end parts of the reeling drum 4 rest with their bearing housings 12 directly on the rails 8. They may alternatively rest on separate rails.
- the press device 48 is arranged to act against the bearing housing 12 during reeling, so that a desired and adjustable linear pressure is maintained in the nip between the surface winding drum 9 and the growing paper reel 3.
- the braking device 50 comprises braking arms 51 with associated actuators and brake linings.
- the cut end of the web is also taped to the surface of the jumbo roll 3 in the braking station 49.
- the braking station 49 also comprises an ejection device 55 which causes the paper real 3 to roll towards the downstream end.
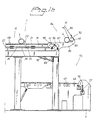
- a stop 56 and a shock absorber 57 are provided at the downstream end of each stand part 6, 7 to restrain the horizontal movement of the paper reel 3 (see Figures 16 and 17).
- a cutting device Upstream of the surface winding drum 9 is a cutting device, not shown, which slits the paper web 2 into two web sections 52, 53, see Figure 5, having substantially the same breadth as the length of the cores 14 threaded onto the reeling drum 4, thus allowing each web section 52, 53 to be reeled onto its own core 14.
- the reel-up also comprises a multi-functional handling station 54 situated at its downstream end for handling finished reels of paper 3, reeling drums 4 and cores 14 therefor.
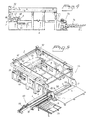
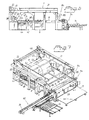
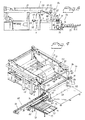
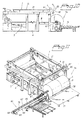
- the handling station 54 comprises a lifting table 58 (see Figure 7) extending between the stand parts 6, 7.
- the lifting table 58 is vertically movable and tiltable with the aid of a plurality of vertical actuators 59 distributed along its long sides.
- the lifting table 58 is provided on its upper side, in the vicinity of the driving side, with suitable sleeve stops 110.
- the lifting table 58 has concave or arched form (see Figure 13) so that the two jumbo rolls 61 formed after withdrawal of the reeling drum 4 are safely retained.
- the lifting table 58 is also arranged, with the help of actuators 59, to tip the jumbo rolls 61 in downstream direction either directly to a suitable transport device (not shown), such as a travelling carriage or a conveyor belt, or to a bench 71 (see Figures 7 and 15) from which the jumbo rolls 61 are then transported further, either to a subsequent work station usually including some type of conversion or rewinding station, or to intermediate storage with the aid of an overhead crane or truck, for instance. The cores are then returned from this station to the reel-up.
- a suitable transport device not shown
- a travelling carriage or a conveyor belt or to a bench 71 (see Figures 7 and 15) from which the jumbo rolls 61 are then transported further, either to a subsequent work station usually including some type of conversion or rewinding station, or to intermediate storage with the
- the handling station 54 further comprises a core-feeding device 72 (see Figure 9) provided with a horizontal, longitudinally extending channel 78 arranged at right angles to the machine direction and situated below the drum moving device 60.
- the channel 78 is open at its inner end, situated in an opening 111 in the stand part 6.
- a feeder 82 is slidably journalled in the channel 78.
- a motor 83 is mounted at the inner end portion of the channel 78 to drive a cogged belt (not shown) which is rigidly connected to the feeder 82 in order to move the feeder 82 to and fro in the channel 78.
- the starting position of the feeder 82 is behind the core 14 and, when actuated, it will press against the rear end of the core 14 to feed it through the opening 111 in the stand part 6 and out onto the lifting table 58.
- One side wall of the channel 78 is provided with an inlet opening 79 which is slightly longer than a core 14.
- the core-feeding device 72 is also provided with a magazine for cores 14 to be used.
- the magazine includes a ramp 73 arranged opposite the inlet opening 79 of the channel 78 and inclined towards this opening.
- the ramp 73 is provided with side plates 75 towards which the ends of the cores face and which serve as guides for the cores 14.
- a stop mechanism 76 (see Figure 8) is arranged at the outlet end of the ramp 73 which in closed position retains the cores 14 on the ramp 73 and in open position allows the lowermost core 14 to roll down into the channel 78, after which it returns to closed position.
- the core-feeding device 72 comprises control equipment (not shown) with associated detectors at the inlet and outlet openings for the stored cores.
- the handling station 54 further comprises a lifting device 84 to lift a reeling drum 4 provided with core(s) from the lifting table 58 to the drum stock 15 at the top of the reel-up (see Figures 8, 9, 16, 17).
- the lifting device 84 comprises two lifting elements 85, in the embodiment shown constituting Z-shaped lifting arms pivotably journalled each in its own support element 19.
- Each lifting arm is made in one piece and has an outer lifting arm part 86, an inner lifting arm part 87 and an inner journalling part 88.
- the two lifting arm parts 86, 87 and the journalling part 88 together form said Z-shape.
- the outer and inner arm parts 86, 87 form an acute angle with each other and define a V-shaped pocket 89 between them for receipt of an end portion of a reeling drum 4.
- the inner lifting arm part 87 and the journalling part 88 form substantially a right angle with each other.
- An actuator 90 in the form of a power cylinder is joined by one end to the inner journalling part 88 spaced from its journalling shaft 112 and with its other end at an attachment element 113 rigidly mounted on the support element 19 (see Figures 8 and 9).
- the force lines of the power cylinders 90 are in their extensions situated at a distance from the journalling shafts 112 of the lifting arms 85 so that the requisite leverage is obtained when activating the lifting arms 85.
- the free end of the outer lifting arm part 86 is provided with an upwardly directed stop 91, seen in the lower starting position of the lifting arm, to retain a reeling drum 4 on the outer lifting arm part 86 when lifting is to commence.
- the lifting arms 85 are joined together by means of a parallel shaft 96, thus ensuring that the lifting arms 85 are turned synchronously.
- the lifting arms 85 are situated in the machine direction and are parallel with each other.
- Their outer and inner lifting arm parts 86, 87 form free edges along which the reeling drum 4 rolls during commencement and completion of the lift.
- a shock absorber 92 (see Figure 17) is arranged at the transition between the outer and inner lifting arm parts 86, 87 in order to prevent the lifting arms 85 from being damaged as a result of the impact energy of the reeling drums 4 against the lifting arms 85, which shock absorber 92 comprises a curved impact absorber 93 and a damping member 94 for this in the form of a hydraulic cylinder.
- a plurality of detectors 40, 41 are arranged on or close to each lifting arm 85 to detect some of the positions of the reeling drum 4 in the lifting arm 85 during its rolling movement therein.
- the detectors 40 are arranged to detect the position of the reeling drum in said V-shaped pocket to obtain a signal for continued lifting of the reeling drum 4 to the level of the rails 21 of the drum stock 15, i.e. the presence of both ends of the reeling drum 4 is registered by the detectors 40.
- the detectors 41 are arranged at the end of the inner journalling part 87 to detect the completion of the lift and subsequent delivery of the reeling drum 4 to the rails 21 of the drum stock 15 so that the lifting arms 85 can return to their lower fetching positions.
- a shock absorber 95 is also arranged at the end of the inner journalling part 87 in order to dampen the rolling-off movement of the reeling drum 4 from the lifting arms 85 onto the rails 21 of the drum stock 15.
- Blocking members 98 are arranged at suitable points along the rails 21, which blocking members 98 are arranged to be folded away under the influence of a reeling drum 4 rolling on the rails and then to return to their blocking position in which the reeling drum 4 is prevented from rolling backwards.
- the blocking members may be provided with springs or counterweights.
- the primary arms 38 are in their upper, receiving position with their gripping members above the surface winding drum 9, said gripping member being open and ready to receive a first reeling drum 4.
- the secondary carriages 42 are in their upstream positions close to the surface winding drum 9.
- a first reeling drum 4 is located on the upper rails 21 above the surface winding drum 9, ready to be gripped by the lowering arms 32, the latter being still in their lowermost position.
- the braking station 49 Downstream in the reel-up 1 the braking station 49 is ready with its braking arm 51, to receive and retard a finished jumbo roll 3.
- the cutting device has been started but is not in production position.
- the first core 14 waits in its feed-in position in the core-feeding device 72 (see Figure 3).
- the lifting table 58 is in its lowermost position and the furthermost core stop 110, in the direction of insertion of the core 14, is set to receive the first core 14 in a position on the lifting table 58 suited for the actual dividing of the paper web 2.
- a reeling drum 4, as yet without a core, is in the feed-in position in the drum moving device 60 at the side of the reel-up.
- the lifting arms 85 are in their lowermost position.
- the feeder 23 of the feeding device 22 is in a ready position at the entry end 99 of the drum stock 15 (see Figure 16).
- the lowering arms 32 move up to the drum stock 15 and the outermost of the reeling drums 4 in the drum stock 15 is lifted over the end stop 30 of the drum stock 15 by the lowering arms 32 (see Figures 1, 14, 15), after which the reeling drum 4 will roll along the roll surfaces 35 of the lowering arms 32 to the shock absorbers 37.
- the detectors 33 indicate when the reeling drum has reached the correct position, whereupon the lowering arms 32 are turned down towards the lowering surfaces 39 (see Figure 14) of the primary system, a distance above the surface winding drum 9, where the gripping devices of the primary arms 38 take over the reeling drum 4.
- the press device 48 and locking device 47 of the primary arms 38 together encompass the reeling drum 4 and position it in its starting position.
- the reeling drum 4 is then accelerated up to the same peripheral speed as that of the surface winding drum 9 in order to minimise the friction when these are brought into contact with each other.
- a wrapping occurs and the paper web 2 is transferred in suitable manner to the reeling drum 4, e.g. the paper reel 3 growing downstream (see Figure 6) can be retarded so that a surplus appears in the web 2 which is drawn into the nip and then cut off.
- the wrapping can be effected by glue or tape having been applied on the cores 14 of the reeling drum 4.
- the secondary carriages 42 While the paper reel 3 is growing the primary arms 38 first and then, after delivery of the reeling drum 4 to the secondary system, the secondary carriages 42, are gradually positioned outwardly from the surface winding drum 9. For the secondary system this means that the secondary carriages 42 move synchronously horizontally along the stand rails 8 (see Figure 6).
- the lifting table 58 and paper reel 3 are raised a short way from the rails 8 of the stand parts 6, 7 so that the reeling drum 4 is free from the stand 5 and the reeling drum 4 can be removed (see Figures 10 to 13) by its braking drum 10 on the operator side 6 being gripped by the gripping members 66 of the drum moving device 60.
- the plates of the reeling drum 4 are loosened, thus disengaging the cores 14, after which the gripping member 66 pulls out the reeling drum 4 to a rest position on the support element 62 (see Figures 11 and 13).
- the jumbo rolls 61 now released on the lifting table 58 are tipped out onto the bench 71 (see Figure 15) by the inner and outer rows of actuators 59 of the lifting table 58 (see Figure 7) being activated in opposite directions.
- a core 14 is caused to roll from the ramp 73 to the channel 78 situated downstream in rolling-out direction.
- the core 14 is then fed along the channel 78 with the aid of the feeder 82 in axial direction to the lifting table 58 (see Figure 5).
- the core stop 110 of the lifting table 58 and its concave shape guarantee that the cores 14 arrive in the correct position on the lifting table 58.
- the actuators 90 of the lifting device 84 are activated during a short interval so that a first initial upward turning movement is achieved.
- the reeling drum 4 is gripped by each stop 91 on the lifting arms 85 and lifted a short distance so that the reeling drum 4 will be caused to roll slowly towards the pockets 89 formed between the outer and inner lifting arm parts 86, 87 (see Figures 8 and 9).
- the lifting table 58 is lowered to its lowermost position by the lifting device 84.
- the impact energy of the drum 4 caused by the rolling is taken up by the shock absorbers 92 (see Figure 17) and when both ends of the reeling drum 4 have thus arrived in said pockets 89, the detectors 40 in the pockets indicate that the drum 4 is in the correct position for lifting.
- the reeling drum 4 passes the blocking members 98 arranged on each rail 21 which, after having been folded aside during passage of the drum, are turned back to their upright blocking positions thereby preventing the reeling drum 4 from rolling back. Finally, the feeders 23 move the reeling drum 4 forward to the outlet 29 of the drum stock 15, either as far as the reeling drums 4 already there or to the end stop 30 (see Figure 17).
- the detectors 31 indicate in the first case that both ends of the reeling drum 4 have reached the correct position.
- the above-mentioned actuators may be hydraulic, pneumatic, electric or mechanical actuators.
- Some or all of the parts of the handling station situated on the operator side may be placed on the drive side of the reel-up if so desired.
- Additional detectors to those described may be arranged at suitable points in the reel-up to detect the beginning or end of various phases or movements during reeling of the paper web and handling the reeling drums, cores and paper reels.
Landscapes
- Replacement Of Web Rolls (AREA)
- Spinning Methods And Devices For Manufacturing Artificial Fibers (AREA)
Claims (9)
- Bobineuse d'une machine à papier pour fabriquer une bande de papier (2) qui est bobinée sur des tambours de bobinage (4) munis de noyaux (14) pour former des bobines (3) de papier, ladite bobineuse ayant une extrémité amont et une extrémité aval et comportant :une paire inférieure de rails parallèles (8) s'étendant à partir de ladite extrémité amont jusqu'à ladite extrémité aval pour supporter un tambour de bobinage (4), dont les parties d'extrémité opposées sont agencées pour rouler le long des rails (8),une paire supérieure de rails parallèles (21) s'étendant à partir de l'extrémité aval jusqu'au voisinage de l'extrémité amont, située au-dessus et espacée par rapport à la paire inférieure de rails (8) pour supporter un stock (15) de tambours de bobinage munis de noyaux, les parties d'extrémité opposées des tambours de bobinage étant agencées pour rouler le long des rails supérieurs (21),un poste de bobinage agencé immédiatement en aval de l'extrémité amont en liaison avec la paire inférieure de rails (8) pour bobiner la bande de papier sur le tambour de bobinage,des dispositifs d'abaissement pour abaisser un tambour de bobinage muni d'un noyau ou de noyaux à partir de la paire supérieure de rails (21) jusqu'audit poste de bobinage,un poste de manipulation multifonctionnel (54) situé à ladite extrémité aval pour manipuler des bobines de papier finies (3), des tambours de bobinage (4) et des noyaux (14), ledit poste de manipulation comportant :une table de levage mobile verticalement (58) pour recevoir chacune des bobines de papier finies,un dispositif (60) pour déplacer un tambour de bobinage (4) à partir d'une bobine de papier située sur la table de levage (58) et pour insérer le tambour de bobinage dans un ou plusieurs noyaux (14) agencés sur la table de levage et alignés avec le dispositif de déplacement de tambour (60) après que la bobine de papier ait été enlevée de la table de levage, etun dispositif pour acheminer des noyaux (14) sur la table de levage (58),ledit poste de manipulation multifonctionnel (54) étant muni d'un dispositif de levage (84) ayant deux éléments de levage (85) agencés pour être amenés en prise avec les parties d'extrémité d'un tambour de bobinage (4) muni d'un ou plusieurs noyaux et situé sur la table de levage (58), et pour lever celui-ci et le mettre sur la paire supérieure de rails (21), et des actionneurs (90) reliés aux éléments de levage (85) pour les déplacer à partir de la table de levage (58) jusqu'au point de fourniture du tambour de bobinage au niveau de la paire supérieure de rails (21), caractérisée en ce que :les éléments de levage (85) sont constitués de bras de levage tourillonnés de manière pivotante dans la bobineuse sur des arbres de tourillonnement fixes permettant la rotation à partir d'une position inférieure de recherche jusqu'à une position supérieure de fourniture, etchacun des bras de levage montés de manière pivotante (85) comporte une partie de bras de levage extérieure (86), une partie de bras de levage intérieure (87) et une partie de tourillonnement intérieure (88), parties de bras de levage (86, 87) le long desquelles le tambour de bobinage (4) est prévu pour rouler, la partie de tourillonnement (88) formant un bras actif relié à une extrémité d'un actionneur (90), dont l'autre extrémité est montée sur les rails supérieurs (21) ou sur un élément de fixation (113) situé au voisinage des rails supérieurs.
- Bobineuse selon la revendication 1, caractérisée en ce que le bras de levage (85) a une forme de Z, les parties de bras de levage extérieure et intérieure (86, 87) formant un angle aigu l'une par rapport à l'autre pour définir une poche en forme de V (89), et en ce que la partie de tourillonnement (8) est agencée sensiblement à angle droit par rapport à la partie de bras de levage intérieure (87).
- Bobineuse selon la revendication 1 ou 2, caractérisée en ce que la partie de bras de levage extérieure (86) du bras de levage (85) est munie d'une butée (91) à son extrémité extérieure libre afin d'assurer que le tambour de bobinage (4) ne roule pas en dehors de la partie de bras de levage extérieure (86) au début du levage.
- Bobineuse selon l'une quelconque des revendications 1 à 3, caractérisée en ce qu'un premier absorbeur de chocs (92) est agencé au niveau d'une transition entre les parties de bras de levage extérieure et intérieure (86, 87), lequel absorbeur de chocs (92) comporte un absorbeur d'impact (93) et un dispositif d'amortissement (94) agencés au niveau de celui-ci.
- Bobineuse selon la revendication 4, caractérisée en ce qu'un second absorbeur de chocs (95) est agencé à la partie d'extrémité de la partie de bras de levage intérieure (87) située la plus proche de la partie de tourillonnement (88) afin d'amortir le mouvement de roulement du tambour de bobinage (4) à partir de la partie de bras de levage (87) jusque sur les rails (21).
- Bobineuse selon l'une quelconque des revendications 1 à 5, caractérisée en ce qu'un arbre parallèle (96) s'étend entre les bras de levage (85), lequel arbre parallèle (96) est agencé pour assurer que les bras de levage (85) sont actionnés de manière synchrone l'un par rapport à l'autre.
- Bobineuse selon l'une quelconque des revendications 1 à 6, caractérisée en ce que ledit poste de manipulation (54) comporte une pluralité de dispositifs de détection pour indiquer diverses positions du tambour de bobinage (4) pour la commande et l'ajustement du mouvement et des positions d'arrêt des éléments de levage (85).
- Bobineuse selon la revendication 7, caractérisée en ce que lesdits dispositifs de détection comportentdes premiers détecteurs (46) agencés pour détecter la présence d'un tambour de bobinage vide (4) muni d'un ou de plusieurs noyaux, afin de déclencher l'activation desdits actionneurs (90) pour amener les éléments de levage (85) en prise avec les parties d'extrémité du tambour de bobinage,des deuxièmes détecteurs (40) agencés pour détecter une position prédéterminée du tambour de bobinage sur les éléments de levage (85) pour déclencher une activation desdits actionneurs (90) pour lever et délivrer le tambour de bobinage à la paire supérieure de rails (21), etdes troisièmes détecteurs (41) pour détecter la fourniture du tambour de bobinage levé (4) pour déclencher l'activation desdits actionneurs (90) pour ramener les éléments de levage (85) vers la position inactive à côté de la table de levage (58).
- Bobineuse selon la revendication 7 ou 8, caractérisée en ce que le poste de manipulation (54) comporte une unité de commande et d'ajustement à laquelle sont connectés les dispositifs de détection (40, 41, 46) et les actionneurs (90), pour activer et désactiver lesdits actionneurs (90).
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| SE9800838A SE511670C2 (sv) | 1998-03-16 | 1998-03-16 | Rullstol i en pappersmaskin |
| SE9800838 | 1998-03-16 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0943569A2 EP0943569A2 (fr) | 1999-09-22 |
| EP0943569A3 EP0943569A3 (fr) | 1999-11-17 |
| EP0943569B1 true EP0943569B1 (fr) | 2003-02-19 |
Family
ID=20410542
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99104106A Expired - Lifetime EP0943569B1 (fr) | 1998-03-16 | 1999-03-01 | Bobineuse |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0943569B1 (fr) |
| AT (1) | ATE232832T1 (fr) |
| DE (1) | DE69905410T2 (fr) |
| SE (1) | SE511670C2 (fr) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN109051936A (zh) * | 2018-08-14 | 2018-12-21 | 珠海市中亚包装设备有限公司 | 送管机 |
| CN116654691A (zh) * | 2023-08-02 | 2023-08-29 | 珠海拾比佰新型材料有限公司 | 一种自动装纸筒设备 |
Families Citing this family (24)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| IT1308270B1 (it) * | 1999-04-12 | 2001-12-10 | Celli Spa | Impianto e metodo per la preparazione di mandrini ed anime diavvolgimento per macchine ribobinatrici o simili |
| WO2003010078A1 (fr) * | 2001-07-26 | 2003-02-06 | Enviroxi, Sl | Procede et dispositif d'evacuation automatique de bobines dans une machine formant lesdites bobines |
| WO2003010079A1 (fr) * | 2001-07-26 | 2003-02-06 | Enviroxi, Sl | Procede et dispositif d'evacuation/introduction automatique de bobines dans une machine de formation/transformation desdites bobines |
| DE10148913A1 (de) * | 2001-10-04 | 2003-04-10 | Voith Paper Patent Gmbh | Verfahren zur Bewegung eines Tambours in einem Tambourmagazin und Tambourmagazin |
| ITMI20012274A1 (it) * | 2001-10-29 | 2003-04-29 | Bielloni Castello S P A | Ribobunatrice automatica particolarmente per film flessibile di materiale plastico e relativo metodo di produzione di rotoli |
| ES2291435T3 (es) * | 2002-03-12 | 2008-03-01 | Dolci Extrusion S.R.L | Bobinadora para pelicula de material elastico. |
| US7255301B2 (en) | 2004-03-01 | 2007-08-14 | Andritz Tissue Inc. | Reel spool storage and loading device and method |
| ITFI20070216A1 (it) * | 2007-09-28 | 2009-03-29 | Celli Paper S P A A | "dispositivo avvolgitore con bracci di sollevamento delle aste di avvolgi- mento" |
| FI125392B (fi) * | 2008-09-29 | 2015-09-30 | Valmet Technologies Inc | Menetelmä ja järjestely rullausakselin laskemiseksi ja/tai nostamiseksi |
| IT1398724B1 (it) | 2010-03-16 | 2013-03-18 | Celli Paper S P A A | "macchina e metodo per l'avvolgimento di bobine di materiale nastriforme" |
| DE102013216494A1 (de) | 2013-08-20 | 2015-02-26 | Voith Patent Gmbh | Vorrichtung zum Transport von Wickelkernen |
| ITMI20131576A1 (it) * | 2013-09-25 | 2015-03-26 | Colines Spa | Gruppo caricatore anime e scarico bobine automatico in una macchina di avvolgimento di film plastico |
| CN103662918B (zh) * | 2013-11-16 | 2016-10-12 | 曹新义 | 复卷机用抽送杆装置 |
| PL3274283T3 (pl) | 2015-03-23 | 2021-12-13 | Roll-O-Matic A/S | Urządzenie do nawijania materiału wstęgowego |
| CN107235382A (zh) * | 2017-07-26 | 2017-10-10 | 威海科莱默自动化设备有限公司 | 一种气胀轴接换辊装置及其接换辊方法 |
| CN107814239B (zh) * | 2017-12-01 | 2023-12-01 | 山东电航电力设备科技有限公司 | 单收带非晶薄带全自动换卷机用卷芯更换装置 |
| CN108341291B (zh) * | 2018-03-30 | 2024-02-02 | 厦门攸信信息技术有限公司 | 直线式卷纸包装机及其控制方法 |
| CN110316592B (zh) * | 2019-08-01 | 2024-03-29 | 上海自立塑料制品有限公司 | 聚酯打包带全自动收卷装置 |
| CN110775685B (zh) * | 2019-12-09 | 2025-04-01 | 温州永塑塑料包装有限公司 | 一种用于送料设备的供料机构 |
| CN111807127B (zh) * | 2020-08-19 | 2025-02-28 | 淄博众成机器人科技有限公司 | 自动换卷装置 |
| CN114476750A (zh) * | 2020-10-23 | 2022-05-13 | 中山润晖机械科技有限公司 | 一种双组份非织造布成套设备 |
| CN114083836B (zh) * | 2021-09-30 | 2024-07-02 | 郑州中南杰特超硬材料有限公司 | 一种用于超硬材料组装的纸管卷成及放置装置 |
| CN114132778B (zh) * | 2021-11-30 | 2024-03-26 | 江苏宏瑞达新能源装备有限公司 | 薄膜展料机 |
| CN117003030A (zh) * | 2023-08-04 | 2023-11-07 | 福建思嘉新材料科技有限公司 | 一种用于pvc地板的卷材生产装置和pvc收卷方法 |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3131880A (en) * | 1962-06-11 | 1964-05-05 | Murray D J Mfg Co | Web roll winder shaft stripper |
| DE3015547C2 (de) * | 1980-04-23 | 1986-12-11 | J.M. Voith Gmbh, 7920 Heidenheim | Wickelmaschine für bahnförmiges Gut |
| DE3040398C2 (de) * | 1980-10-25 | 1984-09-06 | J.M. Voith Gmbh, 7920 Heidenheim | Verfahren zum Auswechseln eines fertigen Wickels gegen einen leeren Wickelkern in einer Doppeltragwalzenwickelmaschine sowie Vorrichtung zur Durchführung des Verfahrens |
| US4682929A (en) * | 1986-02-03 | 1987-07-28 | Hiroshi Kataoka | Device for taking out sheet rolls and mounting sheet roll cores |
| FI75542C (fi) * | 1986-02-27 | 1989-09-11 | Ahlstroem Valmet | Anordning foer foerflyttning av tambourvals till en pappers- eller kartongmaskins rullmaskin. |
| FI73945C (fi) * | 1986-04-03 | 1987-12-10 | Tampella Oy Ab | Anordning foer foerflyttning av en upprullningsvals foer banformigt material fraon ett foerraod till en primaergaffel i en upprullningsanordning vid en pappersmaskin eller liknande. |
| JP2000511861A (ja) * | 1996-06-13 | 2000-09-12 | ビロイト テクノロジーズ、インコーポレイテッド | 巻取機用コア挿入装置 |
-
1998
- 1998-03-16 SE SE9800838A patent/SE511670C2/sv not_active IP Right Cessation
-
1999
- 1999-03-01 DE DE69905410T patent/DE69905410T2/de not_active Expired - Fee Related
- 1999-03-01 EP EP99104106A patent/EP0943569B1/fr not_active Expired - Lifetime
- 1999-03-01 AT AT99104106T patent/ATE232832T1/de active
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN109051936A (zh) * | 2018-08-14 | 2018-12-21 | 珠海市中亚包装设备有限公司 | 送管机 |
| CN109051936B (zh) * | 2018-08-14 | 2024-05-03 | 珠海市中亚科技有限公司 | 送管机 |
| CN116654691A (zh) * | 2023-08-02 | 2023-08-29 | 珠海拾比佰新型材料有限公司 | 一种自动装纸筒设备 |
| CN116654691B (zh) * | 2023-08-02 | 2023-10-13 | 珠海拾比佰新型材料有限公司 | 一种自动装纸筒设备 |
Also Published As
| Publication number | Publication date |
|---|---|
| SE511670C2 (sv) | 1999-11-08 |
| DE69905410T2 (de) | 2003-08-14 |
| EP0943569A2 (fr) | 1999-09-22 |
| EP0943569A3 (fr) | 1999-11-17 |
| SE9800838L (sv) | 1999-09-17 |
| DE69905410D1 (de) | 2003-03-27 |
| ATE232832T1 (de) | 2003-03-15 |
| SE9800838D0 (sv) | 1998-03-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US6047916A (en) | Reel-up and multi-functional handling device therefor | |
| EP0943569A2 (fr) | Bobineuse | |
| US3695539A (en) | Multiple reel unwind stands | |
| US4778122A (en) | Apparatus for transferring reel drums to the winder of a paper or board machine | |
| FI92042B (fi) | Hylsynsyöttölaite | |
| CA1297663C (fr) | Dispositif servant a installer un manchon de bobinage | |
| US4390138A (en) | Reeling apparatus for a web | |
| CA1316893C (fr) | Bobineuse a tension constante avec chargeur automatique de tige de bobineuse | |
| US7255301B2 (en) | Reel spool storage and loading device and method | |
| KR100878464B1 (ko) | 고온의 금속으로 이루어진 열연 예비 스트립의 권취 및권출 장치 | |
| US5360180A (en) | Roll-support system for paper-winding machine | |
| AU603660B2 (en) | Device for unwinding a material web from a roll | |
| US12570490B2 (en) | Plant and method for the movement of cardboard cores | |
| EP1348658A1 (fr) | Dispositif de déroulement de bande pour des rouleaux de bandes | |
| US6016987A (en) | Winding device for a material web, especially for a reel slitting device | |
| CA2066342C (fr) | Dispositif pour le stockage de lamines | |
| US6260788B1 (en) | Reel-up and associated method | |
| EP2511209B1 (fr) | Agencement pour la manipulation de rouleaux de machines et arbres d'enroulement relatifs à la production de réseaux de fibres | |
| EP1126936B1 (fr) | Dispositif pour retirer des bobines de materiau lamine d'une machine de bobinage correspondante | |
| US3695538A (en) | Means for unwinding reels of sheet material | |
| EP1109733B1 (fr) | Appareil permettant de rassembler, de repartir et de stocker des pieces souples laminees, des cuirs industriels notamment | |
| US5480279A (en) | Gripper for handling and storing products in roll form | |
| FI124584B (fi) | Menetelmä ja laite taakkojen käsittelyssä | |
| DE19852978C2 (de) | Druckmaschinenanordnung | |
| JPS63300055A (ja) | シ−トロ−ル取外し装置付きシ−ト分割巻取機 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT DE FR IT |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 20000125 |
|
| AKX | Designation fees paid |
Free format text: AT DE FR IT |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: METSO PAPER KARLSTAD AKTIEBOLAG |
|
| 17Q | First examination report despatched |
Effective date: 20011205 |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Designated state(s): AT DE FR IT |
|
| REF | Corresponds to: |
Ref document number: 69905410 Country of ref document: DE Date of ref document: 20030327 Kind code of ref document: P |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20031120 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20090320 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20090312 Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20101130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101001 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20120330 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20120313 Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 232832 Country of ref document: AT Kind code of ref document: T Effective date: 20130301 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130301 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130301 |