EP0994021B1 - Verfahren und Vorrichtung zum Verpacken von Produkten, und Verpackungsschale dafür - Google Patents
Verfahren und Vorrichtung zum Verpacken von Produkten, und Verpackungsschale dafür Download PDFInfo
- Publication number
- EP0994021B1 EP0994021B1 EP99402467A EP99402467A EP0994021B1 EP 0994021 B1 EP0994021 B1 EP 0994021B1 EP 99402467 A EP99402467 A EP 99402467A EP 99402467 A EP99402467 A EP 99402467A EP 0994021 B1 EP0994021 B1 EP 0994021B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- cavities
- lids
- products
- strip
- heat
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 26
- 238000004806 packaging method and process Methods 0.000 title claims abstract description 17
- 239000000463 material Substances 0.000 claims abstract description 12
- 229920001169 thermoplastic Polymers 0.000 claims abstract description 12
- 239000004416 thermosoftening plastic Substances 0.000 claims abstract description 12
- 238000003466 welding Methods 0.000 claims description 7
- 238000000465 moulding Methods 0.000 claims 2
- 238000003856 thermoforming Methods 0.000 abstract description 13
- 238000007789 sealing Methods 0.000 abstract description 7
- 235000013305 food Nutrition 0.000 abstract description 5
- 239000012815 thermoplastic material Substances 0.000 description 11
- 238000002347 injection Methods 0.000 description 7
- 239000007924 injection Substances 0.000 description 7
- 238000010438 heat treatment Methods 0.000 description 5
- 238000001816 cooling Methods 0.000 description 4
- 239000011324 bead Substances 0.000 description 3
- 239000002184 metal Substances 0.000 description 3
- 238000000926 separation method Methods 0.000 description 3
- 239000000126 substance Substances 0.000 description 3
- 230000005587 bubbling Effects 0.000 description 2
- 230000003750 conditioning effect Effects 0.000 description 2
- 230000007935 neutral effect Effects 0.000 description 2
- 239000000825 pharmaceutical preparation Substances 0.000 description 2
- 229940127557 pharmaceutical product Drugs 0.000 description 2
- 238000007747 plating Methods 0.000 description 2
- 230000001105 regulatory effect Effects 0.000 description 2
- 102000000591 Tight Junction Proteins Human genes 0.000 description 1
- 108010002321 Tight Junction Proteins Proteins 0.000 description 1
- 238000007664 blowing Methods 0.000 description 1
- 238000009835 boiling Methods 0.000 description 1
- 230000001143 conditioned effect Effects 0.000 description 1
- 229910003460 diamond Inorganic materials 0.000 description 1
- 239000010432 diamond Substances 0.000 description 1
- 238000005553 drilling Methods 0.000 description 1
- 239000003814 drug Substances 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 230000005484 gravity Effects 0.000 description 1
- 239000007788 liquid Substances 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 238000012858 packaging process Methods 0.000 description 1
- 235000010603 pastilles Nutrition 0.000 description 1
- 238000011084 recovery Methods 0.000 description 1
- 210000001578 tight junction Anatomy 0.000 description 1
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B9/00—Enclosing successive articles, or quantities of material, e.g. liquids or semiliquids, in flat, folded, or tubular webs of flexible sheet material; Subdividing filled flexible tubes to form packages
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D77/00—Packages formed by enclosing articles or materials in preformed containers, e.g. boxes, cartons, sacks or bags
- B65D77/22—Details
- B65D77/30—Opening or contents-removing devices added or incorporated during filling or closing of containers
Definitions
- the invention relates to a process for packaging products, including food, chemical or pharmaceutical products, to a device for implementing said method, as well as a tray of packaging of products.
- Product storage can be extended by packaging products in vacuum or inert atmosphere, by injection of a neutral gas at the welding station.
- the document EP 0 652 155 A1 describes a method, a device and a packaging container for food, chemical or pharmaceuticals using a first strip of thermoplastic material or thermoformable and a second strip of thermoplastic material or heat-sealable.
- the invention also relates to a device for conditioning products in thermoformed trays, using a single strip of thermoplastic or thermoformable material, comprising means for thermoforming of cavities and associated covers in said strip, means of cutting on three sides around the covers, means of loading the cavities with products, means for folding the covers on the cavities and means for heat sealing the covers to cavities for constituting trays containing said products;
- the invention also relates to a packaging tray of products obtained by implementing a method according to the invention in using a device according to the invention.
- the cavity and the cover have edges with distinct contours, so that provide two tabs capable of being separated to facilitate the opening of the tray.
- a device according to the invention is consisting of online assembly of functional modules supported by load-bearing frames for treating a single strip of thermoplastic material or thermoformable unwound from a roll 1.
- the means of gripping and driving the first strip of thermoplastic material constituted by the horizontal chains are in themselves known, in particular by document FR 2.027.741 in the name of applicant for this application, and do not require further description Detailed.
- thermoplastic strip of roll 1 is unwound flat to arrive in a first zone 2 adapted to receive a device 3 of preheating of the strip of thermoplastic material.
- Preheating is performed for example by means of one or more metal plates having good thermal conductivity.
- metal plates having good thermal conductivity.
- a heating element for example a armored resistor electrically insulated from the metal plate.
- thermoforming zone 4 comprising a thermoforming module 5.
- thermoforming technique used in zone 4 of thermoforming is for example the thermoforming technique known as "negative" simple ", the most common technique in which we first heating the strip of material to be thermoformed by applying it to the contact of a heating plate 5a, then the actual deformation by blowing compressed air through an upper heating plate 5b provided with this effect of appropriate orifices.
- thermoforming module 5 could comply to the technique known as "negative with mechanical assistance", technique in which the film is heated by a contact on either side of this by sandwiching between two thermally regulated plates possibly at different temperatures, then by lowering a piston for example metallic to pre-stretch the strip of performed material and finally by plating the thermoplastic strip on the mold by air injection or compressed gas through the piston provided for this purpose with suitable orifices.
- negative with mechanical assistance technique in which the film is heated by a contact on either side of this by sandwiching between two thermally regulated plates possibly at different temperatures, then by lowering a piston for example metallic to pre-stretch the strip of performed material and finally by plating the thermoplastic strip on the mold by air injection or compressed gas through the piston provided for this purpose with suitable orifices.
- thermoforming line is constituted in double line allowing the simultaneous conditioning in parallel of two trays.
- Each hollow cover A is thus detached from the strip on three sides by only being connected to the strip of thermoformable material by the aforementioned fasteners.
- Guide rails or pads are advantageously provided to support and guide the covers A driven by advancing in successive steps the strip of thermoplastic material.
- the cavities B are filled in a zone 10 for filling products to be packaged, or manually, either by 11 pouring or dosing devices.
- the covers A are folded down over the cavities B around the aforementioned fasteners in a drawdown zone 12 thanks to a medium 13 lid flap.
- thermoformable strip in which the mechanical elements located above of the thermoformable strip have not been shown for clarity, we finds that the folding of the covers A in the area 12 shows contours cut C in the thermoformable strip.
- the covers A folded down and cavities B are then entrained in a welding zone 14, in which two welding bells 15a, 15b come apply to the edges of the covers A and cavity B to weld them so as to make a tight junction.
- the module heat sealing 15a, 15b optionally incorporates an underlayer vacuum depending on the nature of the materials to be welded and the products to be contain (indeed, for certain emulsified products or with a high content of liquid, you can only carry out a partial vacuum under penalty of boiling the product to be packaged).
- the trays are cooled sealed containing the product packaged in a zone 16 of cooling, in which two cooling bells 17a, 17b cool the trays, and in particular the tray edges which have just been welded in zone 14.
- thermoplastic strip At this stage, the cooled trays are still attached to the thermoplastic strip, because the edges of cavities B have not been detached from the thermoplastic strip.
- This separation is carried out in the final cutting zone 18 at by means of cutting discs 19a, 19b counter-rotating.
- Discs 19a, 19b cut the edges of the edges of cavities A, which are wound on recovery drums 20.
- thermoforming phase of zone 4 carried out in module 5 to simultaneously constitute a cavity B and a cover A in the strip of thermoplastic material advancing step by step in advance predetermined according to the dimensions of the corresponding mold.
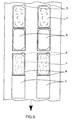
- FIG. 9 represents a preferred embodiment of the invention and illustrates with references identical to those of the preceding figures the setting implementation of the invention by folding the covers A over the cavities B filled with product P, so as to release in the thermoformed strip contours C cut out of separation between successive trays.
- FIG. 10 schematically represents an embodiment preferred tray according to the invention.
- the cover A has rectangular flanges 22 which protrude rounded edges of cavity B while cavity B has a tongue 23 able to be moved away from the corner 22 to allow by simple pull easy opening of the tray.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Containers And Plastic Fillers For Packaging (AREA)
- Packages (AREA)
- Basic Packing Technique (AREA)
- Container Filling Or Packaging Operations (AREA)
Claims (10)
- Verfahren zum Verpacken von Produkten (P) in Schalen, die aus einem Endlosstreifen aus thermoplastischem oder warmverformbarem Werkstoff (1) durch Warmverformen hergestellt werden, wobei das Verfahren die Arbeitsschritte umfasst: Warmformung (4) von Hohlräumen (B) und von damit verbundenen Deckeln (A) in diesem Streifen, Abtrennen an drei Seiten um die Deckel (A) herum, wobei die Hohlräume mit diesem Streifen fest verbunden bleiben, Befüllen (10) der Hohlräume (B) mit Produkten (P), Umklappen (12) der Deckel (A) auf die Hohlräume (B) und Warmverschweißen (14) der Deckel (A) auf den Hohlräumen (B), um Schalen zu bilden, die diese Produkte (P) enthalten.
- Verfahren nach Anspruch 1, das ferner einen Arbeitsschritt (6) des Vorschneidens zwischen Hohlräumen (B) und den zugehörigen Deckeln (A) umfasst, um eine oder mehrere Verbindungen stehen zu lassen, die als Scharnier zum Umklappen dienen.
- Verfahren nach Anspruch 1 oder Anspruch 2, das ferner einen Arbeitsschritt des Abschneidens (18) von Randleisten umfasst, die um die Hohlräume (B) umlaufen, die mit den Deckeln (A) warmverschweißt werden, so dass eine oder mehrere Schalen, die diese Produkte (P) enthalten, einzeln herausgenommen werden können.
- Vorrichtung zur Ausführung des Verfahrens nach Anspruch 1, die Mittel (5) zum Warmformen von Hohlräumen (B) und zugehörigen Deckeln (A) aus dem genannten Streifen, Mittel zum Abtrennen an drei Seiten (9a, 9b) um die Deckel (A) herum, Mittel zum Befüllen (11) der Hohlräume mit Produkten (P), Mittel zum Umklappen (13) der Deckel (A) auf die Hohlräume (B) sowie Mittel zum Warmverschweißen der Deckel (A) auf den Hohlräumen (B), um Schalen zu bilden, die diese Produkte (P) enthalten, umfasst.
- Vorrichtung nach Anspruch 4, die Mittel (7a, 7b) zum Vorschneiden zwischen Hohlräumen (B) und zugehörigen Deckeln (A) umfasst, um eine oder mehrere Verbindungen stehen zu lassen, die als Scharnier zum Umklappen dienen.
- Vorrichtung nach Anspruch 4 oder Anspruch 5, die Mittel (19a, 19b) zum Abschneiden von Randleisten umfasst, die um die Hohlräume (B) umlaufen, die mit den Deckeln (A) warmverschweißt werden.
- Vorrichtung nach einem der Ansprüche 4 bis 6, bei der die Mittel zum Umklappen (13) der Deckel (A) auf die Hohlräume (B) mindestens einen einziehbaren Drehfinger umfassen.
- Vorrichtung nach einem der Ansprüche 4 bis 7, bei der die Mittel zum Umklappen (13) der Deckel (A) auf die Hohlräume (B) dazu vorbestimmt sind, die Deckel zu heben und sie um einen Winkel von mehr als 90° umzuklappen.
- Verpackungsschale für Produkte, die durch die Ausführung eines Verfahrens nach einem der Ansprüche 1 bis 3 bzw. unter Verwendung einer Vorrichtung nach einem der Ansprüche 4 bis 7 hergestellt wird.
- Verpackungsschale nach Anspruch 9,
dadurch gekennzeichnet, dass der Hohlraum (B) und der Deckel (A) Ränder mit unterschiedlichen Konturen aufweisen, die so dass zwei Laschen (22, 23) gebildet werden, die auseinandergespreizt werden können, um das Öffnen der Schale zu erleichtern.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9812981 | 1998-10-16 | ||
| FR9812981A FR2784654B1 (fr) | 1998-10-16 | 1998-10-16 | Procede et dispositif de conditionnement de produits et barquettes de conditionnement correspondantes |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0994021A1 EP0994021A1 (de) | 2000-04-19 |
| EP0994021B1 true EP0994021B1 (de) | 2003-12-10 |
Family
ID=9531639
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99402467A Expired - Lifetime EP0994021B1 (de) | 1998-10-16 | 1999-10-08 | Verfahren und Vorrichtung zum Verpacken von Produkten, und Verpackungsschale dafür |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US6282870B1 (de) |
| EP (1) | EP0994021B1 (de) |
| AT (1) | ATE256031T1 (de) |
| DE (1) | DE69913462T2 (de) |
| ES (1) | ES2213341T3 (de) |
| FR (1) | FR2784654B1 (de) |
Families Citing this family (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US20020096431A1 (en) * | 1999-09-01 | 2002-07-25 | Pierre Sevigny | Apparatus for the manufacture of a disposable electrophoresis cassette and method thereof |
| DK1214244T3 (da) * | 1999-09-09 | 2004-07-12 | Dairygold Technologies Ltd | Fremgangsmåde til at emballere födevareprodukter |
| DE10033796C1 (de) * | 2000-07-12 | 2001-10-11 | Illig Maschinenbau Adolf | Verfahren zum Herstellen von Standblisterpackungen und Vorrichtung zur Durchführung des Verfahrens |
| US7244221B2 (en) * | 2004-05-21 | 2007-07-17 | Rogar Capital Corporation | Method and apparatus for simultaneously forming an articulable container with fold creases |
| US7987655B2 (en) * | 2008-04-22 | 2011-08-02 | Rovema Packaging Machines, Lp | Tubular bagging machine and method |
| FR2961428B1 (fr) * | 2010-06-18 | 2013-04-26 | Sidel Participations | Module porte-outils pour le faconnage d'au moins une decoupe de carton |
| DE102013204160A1 (de) * | 2013-03-11 | 2014-09-11 | Multivac Sepp Haggenmüller Gmbh & Co. Kg | Verpackungsanlage mit Einraststation und Verfahren |
| CN105690820B (zh) * | 2016-01-27 | 2018-05-04 | 蚌埠市众邦包装厂 | 一种立式浅底压塑包装盒连续性加工装置 |
| CN105643964B (zh) * | 2016-01-27 | 2018-01-23 | 蚌埠市众邦包装厂 | 一种卧式浅底压塑包装盒连续性加工设备 |
| CN105563795B (zh) * | 2016-01-27 | 2018-03-27 | 蚌埠市众邦包装厂 | 一种卧式浅底压塑包装盒加工控制系统 |
| JP6152201B1 (ja) * | 2016-06-29 | 2017-06-21 | Ckd株式会社 | ブリスタ包装機 |
| WO2018129124A1 (en) * | 2017-01-04 | 2018-07-12 | Church & Dwight Co., Inc. | A system and a related method for forming a multi-chamber package |
| WO2020041008A1 (en) | 2018-08-21 | 2020-02-27 | Intercontinental Great Brands Llc | Food storage tray |
| USD964862S1 (en) | 2018-08-21 | 2022-09-27 | Intercontinental Great Brands Llc | Tray |
| CN118977403B (zh) * | 2024-10-21 | 2024-12-20 | 新创源云海(成都)科技有限公司 | 一种高效连续生产载带短节的生产装置及方法 |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB1286151A (en) | 1969-01-03 | 1972-08-23 | Lucas Industries Ltd | Plunger operated switches |
| SE434131B (sv) | 1979-09-12 | 1984-07-09 | Tetra Pak Int | Sett vid framstellning av behallare avsedd for ett under overtryck staende fyllgods, samt behallare for ett under overtryck staende fyllgods |
| US4387551A (en) * | 1979-09-21 | 1983-06-14 | Maryland Cup Corporation | Heat-sealable, ovenable containers and method of manufacture |
| US5007231A (en) * | 1985-08-16 | 1991-04-16 | Plm Ab | Container |
| US5009056A (en) * | 1987-01-16 | 1991-04-23 | Porteous Don D | Method for preparing finger mountable dispensing cups |
| US5369937A (en) * | 1993-05-10 | 1994-12-06 | Joule' Inc. | Continuous casting and packaging |
| US5419096A (en) * | 1993-07-28 | 1995-05-30 | World Class Packaging Systems, Inc. | Packaging method and apparatus for packaging large meat products in a desired gaseous atmosphere |
| FR2712253B1 (fr) * | 1993-11-10 | 1996-01-19 | Mecaplastic | Procédé et dispositif de conditionnement de produits alimentaires, chimiques ou pharmaceutiques et barquettes de conditionnement correspondantes. |
| US5496250A (en) * | 1994-04-25 | 1996-03-05 | Fielder; Larry D. | Method for forming tray type cartons |
-
1998
- 1998-10-16 FR FR9812981A patent/FR2784654B1/fr not_active Expired - Fee Related
-
1999
- 1999-10-08 ES ES99402467T patent/ES2213341T3/es not_active Expired - Lifetime
- 1999-10-08 EP EP99402467A patent/EP0994021B1/de not_active Expired - Lifetime
- 1999-10-08 DE DE69913462T patent/DE69913462T2/de not_active Expired - Lifetime
- 1999-10-08 AT AT99402467T patent/ATE256031T1/de not_active IP Right Cessation
- 1999-10-18 US US09/419,802 patent/US6282870B1/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| FR2784654A1 (fr) | 2000-04-21 |
| ES2213341T3 (es) | 2004-08-16 |
| US6282870B1 (en) | 2001-09-04 |
| ATE256031T1 (de) | 2003-12-15 |
| FR2784654B1 (fr) | 2001-01-12 |
| DE69913462T2 (de) | 2004-10-07 |
| DE69913462D1 (de) | 2004-01-22 |
| EP0994021A1 (de) | 2000-04-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0652155B1 (de) | Verfahren und Vorrichtung zum Verpacken von Lebensmitteln, chemischen oder pharmazeutischen Produkten und Verpackungsschale dafür | |
| EP2956292B1 (de) | Verpackung von einer gruppe mit mindestens zwei kunststoffbehältern | |
| EP0994021A1 (de) | Verfahren und Vorrichtung zum Verpacken von Produkten, und Verpackungsschale dafür | |
| EP0252791B1 (de) | Präsentationsschale in der Form eines Behälters | |
| FR2464815A1 (fr) | Procede de fabrication d'un emballage etanche aux gaz | |
| EP3481737B1 (de) | Mit biopharmazeutischen flüssigkeiten zu befüllender, flexibler 3d-beutel und verfahren zur herstellung solch eines beutels | |
| WO1986002055A1 (fr) | Emballage etanche, procede de fabrication et utilisation de cet emballage | |
| WO2013057392A1 (fr) | Procede de fabrication d'une boîte de conditionnement et boite obtenue selon ce procede | |
| FR2503036A1 (fr) | Bande composite a couvercles pour recipients thermoplastiques et procede, dispositif et installation de fabrication d'une telle bande composite | |
| US6719015B2 (en) | Apparatus and process for manufacturing a filled flexible pouch | |
| CH621744A5 (de) | ||
| EP0388310A1 (de) | Einzelpackung zum Verpacken von Lebensmitteln sowie Verfahren und Vorrichtung zu ihrer Herstellung | |
| EP2238037B1 (de) | Verfahren zur verpackung eines pastenprodukts in einer leicht zu öffnenden versiegelten verpackung aus kunststoffmaterial | |
| CH626561A5 (en) | Method for the manufacture of an assembly formed by a covering sheet and a support, device for implementing the method, and container obtained | |
| EP0062571B1 (de) | Durchstechvorrichtung und -verfahren für Behälterverschluss und Einrichtung zur Herstellung der Vorrichtung | |
| FR2763015A1 (fr) | Procede de soudage de feuilles thermoformees de matiere plastique et machine pour la mise en oeuvre de ce procede | |
| EP1340678A1 (de) | Dichter Lebensmittelbehälter | |
| EP1432616B1 (de) | Vorrichtung zum folienverschliessen von verpackungen in einer maschine zum konditionieren unter kontrollierter atmosphäre | |
| EP2722155A1 (de) | Vorrichtung zur Herstellung von Behältern durch Warmformen | |
| BE900166A (fr) | Conditionnement etanche pour tres petites doses de liquides, pates ou poudres. | |
| FR2663910A1 (fr) | Bande composite et installation pour la fabrication d'emballages steriles thermoformes. | |
| CH619408A5 (en) | Method for packaging in a sterile environment and installation for implementing the method | |
| FR2914278A1 (fr) | Procede et dispositif de conditionnement de denrees perissables tels les fruits. | |
| EP0885805A1 (de) | Verfahren und Vorrichtung zum Thermoformen, Füllen und Verschliessen von Kunststoffbechern | |
| FR2898339A1 (fr) | Procede et machine de formage et de thermoscellage d'un film plastique sur un article tel qu'une boite sterile pour la culture de micro-organismes, et article ainsi obtenu |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17P | Request for examination filed |
Effective date: 20000930 |
|
| AKX | Designation fees paid |
Free format text: AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031210 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20031210 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031210 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031210 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031210 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20031210 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: FRENCH |
|
| REF | Corresponds to: |
Ref document number: 69913462 Country of ref document: DE Date of ref document: 20040122 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040310 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040310 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20040310 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20040324 |
|
| NLV1 | Nl: lapsed or annulled due to failure to fulfill the requirements of art. 29p and 29m of the patents act | ||
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2213341 Country of ref document: ES Kind code of ref document: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041008 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041031 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041031 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041031 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20041031 |
|
| 26N | No opposition filed |
Effective date: 20040913 |
|
| BERE | Be: lapsed |
Owner name: *MECAPLASTIC Effective date: 20041031 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| BERE | Be: lapsed |
Owner name: *MECAPLASTIC Effective date: 20041031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040510 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20101022 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20101021 Year of fee payment: 12 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20111103 Year of fee payment: 13 Ref country code: ES Payment date: 20111026 Year of fee payment: 13 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20121008 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20130628 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20121008 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130501 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 69913462 Country of ref document: DE Effective date: 20130501 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20121031 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20140116 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20121009 |