EP0997247B1 - Matrice d'extrusion pour la fabrication de corps en nid d'abeilles - Google Patents
Matrice d'extrusion pour la fabrication de corps en nid d'abeilles Download PDFInfo
- Publication number
- EP0997247B1 EP0997247B1 EP99308568A EP99308568A EP0997247B1 EP 0997247 B1 EP0997247 B1 EP 0997247B1 EP 99308568 A EP99308568 A EP 99308568A EP 99308568 A EP99308568 A EP 99308568A EP 0997247 B1 EP0997247 B1 EP 0997247B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- die
- slit
- axis
- open ends
- taper portion
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000004519 manufacturing process Methods 0.000 title claims description 23
- 230000002093 peripheral effect Effects 0.000 claims description 10
- 230000037303 wrinkles Effects 0.000 description 6
- 239000000919 ceramic Substances 0.000 description 5
- 230000000052 comparative effect Effects 0.000 description 5
- 238000010276 construction Methods 0.000 description 4
- 239000000463 material Substances 0.000 description 4
- 238000001125 extrusion Methods 0.000 description 3
- 125000006850 spacer group Chemical group 0.000 description 3
- 238000002474 experimental method Methods 0.000 description 2
- 229910052878 cordierite Inorganic materials 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- JSKIRARMQDRGJZ-UHFFFAOYSA-N dimagnesium dioxido-bis[(1-oxido-3-oxo-2,4,6,8,9-pentaoxa-1,3-disila-5,7-dialuminabicyclo[3.3.1]nonan-7-yl)oxy]silane Chemical compound [Mg++].[Mg++].[O-][Si]([O-])(O[Al]1O[Al]2O[Si](=O)O[Si]([O-])(O1)O2)O[Al]1O[Al]2O[Si](=O)O[Si]([O-])(O1)O2 JSKIRARMQDRGJZ-UHFFFAOYSA-N 0.000 description 1
- 239000002075 main ingredient Substances 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 238000011176 pooling Methods 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B28—WORKING CEMENT, CLAY, OR STONE
- B28B—SHAPING CLAY OR OTHER CERAMIC COMPOSITIONS; SHAPING SLAG; SHAPING MIXTURES CONTAINING CEMENTITIOUS MATERIAL, e.g. PLASTER
- B28B3/00—Producing shaped articles from the material by using presses; Presses specially adapted therefor
- B28B3/20—Producing shaped articles from the material by using presses; Presses specially adapted therefor wherein the material is extruded
- B28B3/26—Extrusion dies
- B28B3/269—For multi-channeled structures, e.g. honeycomb structures
Definitions
- the present invention relates to a die for manufacturing honeycomb bodies used for extruding honeycomb structural bodies.
- various kinds of dies for manufacturing honeycomb bodies which comprise; a die main body including batch supply holes which are opened to a backside surface of the die, slit channels which are communicated with the batch supply holes and are opened to a foreside surface of the die and a taper worked portion which is formed by working an outer peripheral portion of the foreside surface of the die in a taper manner; and a control plate arranged at a portion opposed to the taper worked portion.
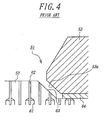
- Fig. 4 is a schematic view showing one embodiment of a known die for manufacturing honeycomb bodies.
- a die 51 for manufacturing honeycomb bodies comprises a die main body 52 and a control plate 53.
- the die main body 52 has a disk-shape and comprises batch supply holes 61 which are opened to its backside surface (lower surface (not shown) in Fig. 4) and slit channels 62 which are opened to its foreside surface (upper surface in Fig. 4).
- the slit channels 62 have a crisscross shape at the foreside surface of the die main body 52, and the batch supply holes 61 are communicated with alternate intersection points.
- An outer peripheral portion of the die main body 52 is worked into a taper shape to form a taper worked portion 63.
- the control plate 53 is connected to the die main body 52 via a spacer 64 in such a manner that one surface 53a is opposed (parallel in Fig. 4) to the taper worked portion 63.
- a ceramic batch for example is supplied from the batch supply holes 61 which are opened to the backside surface of the die 51, and the thus supplied ceramic batch is extruded from the slit channels 62 which are opened to the foreside surface of the die 51, so as to obtain a honeycomb structural body. Then, it is possible to reduce an inward batch stress when an outer wall is formed and to prevent a collapsing of outer cells i.e. a generation of wrinkle portions in the honeycomb structural body by forming the taper worked portion 63 at the outer peripheral portion of the die main body 52 and by arranging the control plate 53 at a portion opposed to the taper worked portion 63.
- US 4349329 teaches an extrusion due having grid-shaped extrusion slots and a die mask which covers the outer peripheral portion of the die on the extrudable material outlet side.
- the extrusion slots at the periphery of the uncovered area are tapered outwardly towards their open ends.
- a pooling zone is provided in the covered area to provide extrudable material to the uncovered slots.
- An object of the invention is to eliminate the drawbacks mentioned above and to provide a die for manufacturing honeycomb bodies in which a rib strength can be improved and a generation of wrinkle portions at an outer portion, which is a fatal defect of a thin honeycomb body, can be prevented.
- the slit channel expanding portions having the construction mentioned above are arranged at a predetermined portion of the slit channels existing in the taper worked portion of the outer peripheral portions, a larger amount of batch can be supplied to the slit channel expanding portions as compared with that of the other portion, and thus the outermost ribs of the honeycomb structural body can be strengthened. Therefore, an isostatic strength of the honeycomb structural body can be improved even if the honeycomb structural body has a thin wall, and it is possible to prevent a generation of wrinkle portions at the outer portion.
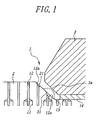
- Fig. 1 is a schematic view showing one embodiment of a die for manufacturing honeycomb bodies according to the invention.
- a die 1 for manufacturing honeycomb bodies comprises a die main body 2 and a control plate 3.
- the die main body 2 has a disk-shape and comprises batch supply holes 11 which are opened to its backside surface (lower surface (not shown) in Fig. 1) and slit channels 12 which are opened to its foreside surface (upper surface in Fig. 1).
- the slit channels 12 have a crisscross shape at the foreside surface of the die main body 2, and the batch supply holes 11 are communicated with alternate intersection points.
- An outer peripheral portion of the die main body 2 is worked into a taper shape to form a taper worked portion 13.
- the control plate 3 is connected to the die main body 2 via a spacer 14 in such a manner that one surface 3a is opposed (parallel in Fig. 1) to the taper worked portion 13.
- the construction of the die 1 for manufacturing honeycomb bodies according to the invention mentioned above is the same as that of the known die for manufacturing honeycomb bodies.
- a different point between the die 1 according to the invention and the known die is that slit channel expanding portions are formed at open ends of the slit channels 12 existing in the taper worked portion 13 of the outer peripheral portion of the die main body 2.
- the slit channel expanding portion 21 the slit channel 12 is expanded gradually toward an open end 12a.
- the slit channel expanding portion 21 is formed by performing a C-chamfer working for the open end 12a of the slit channel 12.
- the C-chamfer working can be performed by grinding the slit channel 12 by means of a whetstone which is set with a predetermined angle with respect to the open end 12a of the slit channel 12. Moreover, the slit channel expanding portion 21 is formed locally by a constant distance from the open end 12a of the slit channel 12.
- the slit channel expanding portions 21 are arranged at a predetermined position, a larger amount of batch can be extruded from the slit channels 12, in which the slit channel expanding portions 21 are arranged, as compared with the slit channels 12 in which no slit channel expanding portions 21 are arranged.
- the batch extruded from the slit channel expanding portions 21, whose amount is larger than that of the other portion, is contacted to the control plate 2 and then integrated inwardly.
- the honeycomb structural body after forming it is possible to strengthen the ribs existing the outer peripheral portion thereof.
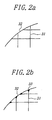
- Figs. 2a and 2b One example is shown in Figs. 2a and 2b. Fig.
- Fig. 2 shows a part of the honeycomb structural body extruded by using the known die for manufacturing honeycomb bodies.
- Fig. 2b illustrates a part of the honeycomb structural body extruded by using the die 1 for manufacturing honeycomb bodies according to the invention. The following is understood from a comparison between Fig. 2a and Fig. 2b.
- reinforced portions 33 are formed at connecting portions between ribs 31 and an outer wall 32 and thus an isostatic strength of the honeycomb structural body can be improved.
- the wrinkle portions are not generated at the outer portion.
- the slit channel expanding portion 21 is formed by performing a C-chamfer on the open end 12a of the slit channel 12.
- This C-chamfer working can form the slit channel expanding portions 21 at an easiest manner.
- the present invention is not limited to the C-chamfer working and it is possible to use other working methods if they can expand the slit channel 12 as mentioned above.
- materials of the die main body 2, the control plate 3 and the spacer 14 are not explained, but it is a matter of course that the same materials used in the known die such as stainless can be used.
- ceramic honeycomb structural bodies made of cordierite as a main ingredient, having a dimension of diameter: 103 mm, length: 100 mm, wall thickness: 75 ⁇ m (3 mil), cell number: 62 cells per square centimetre (400 cpsi) were extruded by using dies according to a comparative example and examples 1-2 to form ceramic honeycomb structural bodies. Then, with respect to the thus formed ceramic honeycomb structural bodies, ISO (isostatic) strengths in a radial direction were measured and compared.
- ISO isostatic
- the slit channel expanding portions having the construction mentioned above are arranged at a predetermined portion of the slit channels existing in the taper worked portion of the outer peripheral portions, a larger amount of batch can be supplied to the slit channel expanding portions as compared with that of the other portion, and thus the outermost ribs of the honeycomb structural body can be strengthened. Therefore, an isostatic strength of the honeycomb structural body can be improved even if the honeycomb structural body has a thin wall, and it is possible to prevent a generation of wrinkle portions at the outer portion.
Landscapes
- Engineering & Computer Science (AREA)
- Manufacturing & Machinery (AREA)
- Chemical & Material Sciences (AREA)
- Ceramic Engineering (AREA)
- Mechanical Engineering (AREA)
- Press-Shaping Or Shaping Using Conveyers (AREA)
Claims (4)
- Matrice (1) pour la fabrication de corps de nids d'abeilles comprenant :caractérisée en ce que :un corps principal de matrice (2) comportant des trous d'alimentation discontinue (11) qui s'ouvrent sur une surface arrière de la matrice (1) ;des gorges fendues (12) en communication avec les trous d'alimentation discontinue (11) et ouverts sur une surface avant de la matrice (1) ;une portion conique (13) formant une partie périphérique externe de la surface avant de la matrice (1) de manière conique ; etune pla que de commande (3) placée dans une position opposée à la portion conique (13) ;les gorges fendues (12) s'ouvrant dans la portion conique (13) comportent des portions de dilatation de gorges fendues (21) formées à leurs extrémités ouvertes (12a) de telle manière que les gorges fendues (12) se dilatent graduellement vers leurs extrémités ouvertes (12a).
- Matrice (1) pour la fabrication de corps de nids d'abeilles selon la revendication 1, dans laquelle chacune desdites portions de dilatation de gorges fendues (21) est un chanfrein en forme de C aux extrémités ouvertes de la gorge fendue (12).
- Matrice (1) pour la fabrication de corps de nids d'abeilles selon la revendication 2, dans laquelle :les gorges fendues (12) ont une forme entrecroisée sur la surface avant du corps principal de matrice (2), la direction des lignes de l'entrecroisement définissant respectivement un axe X et un axe Y ; etlesdites portions de dilatation de gorges fendues (21) sont prévues aux extrémités ouvertes de toutes les gorges fendues (12) s'ouvrant dans la portion conique (13) et s'étendant le long de l'axe X et aux extrémités ouvertes de toutes les gorges fendues (12) s'ouvrant dans la portion conique (13) et s'étendant le long de l'axe Y.
- Matri ce (1) pour la fabrication de corps de nids d'abeilles selon la revendication 2, dans laquelle :les gorges fendues (12) ont une forme entrecroisée sur la surface avant du corps principal de matrice (2), la direction des lignes de l'entrecroisement définissant respectivement un axe X et un axe Y ; etlesdites portions de dilatation de gorges fendues (21) sont prévues dans différentes régions circonférentielles respectives (41, 42, 43) de la portion conique , (a) aux extrémités ouvertes uniquement des gorges fendues (12) s'ouvrant dans la portion conique (13) e t s'étendant le long de l'axe X, (b) aux extrémités ouvertes uniquement des gorges fendues (12) s'ouvrant dans la portion conique (13) et s'étendant le long de l'axe Y, et (c) aux extrémités ouvertes des gorges fendues (12) s'ouvrant dans la portion conique (13) et s'étendant le long de l'axe X et aux extrémités ouvertes des gorges fendues (12) s'ouvrant dans la portion conique (13) et s'étendant le long de l'axe Y.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP30880298A JP3701801B2 (ja) | 1998-10-29 | 1998-10-29 | ハニカム製造用口金 |
| JP30880298 | 1998-10-29 |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP0997247A2 EP0997247A2 (fr) | 2000-05-03 |
| EP0997247A3 EP0997247A3 (fr) | 2002-05-29 |
| EP0997247B1 true EP0997247B1 (fr) | 2004-08-18 |
Family
ID=17985495
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99308568A Expired - Lifetime EP0997247B1 (fr) | 1998-10-29 | 1999-10-28 | Matrice d'extrusion pour la fabrication de corps en nid d'abeilles |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US6287103B1 (fr) |
| EP (1) | EP0997247B1 (fr) |
| JP (1) | JP3701801B2 (fr) |
| DE (1) | DE69919483T2 (fr) |
Families Citing this family (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2002283326A (ja) * | 2001-03-28 | 2002-10-03 | Ngk Insulators Ltd | ハニカム構造体成形装置及び成形方法 |
| JP4210446B2 (ja) | 2001-09-19 | 2009-01-21 | 日本碍子株式会社 | ハニカム押出成形用口金及びその製造方法 |
| WO2004073969A2 (fr) * | 2003-02-18 | 2004-09-02 | Corning Incorporated | Corps alveolaire ceramique et procede de fabrication |
| US7112050B2 (en) * | 2003-06-26 | 2006-09-26 | Corning Incorporated | Extrusion die for making a double-skin honeycomb substrate |
| US7914724B2 (en) | 2005-07-29 | 2011-03-29 | Corning Incorporated | Methods for extruding a honeycomb article with a skin surrrounding a central cellular structure |
| KR100855167B1 (ko) * | 2005-11-18 | 2008-08-29 | 이비덴 가부시키가이샤 | 벌집형 구조체 |
| CN100560180C (zh) * | 2005-11-18 | 2009-11-18 | 揖斐电株式会社 | 蜂窝结构体 |
| EP2127836B1 (fr) * | 2007-02-01 | 2013-12-11 | NGK Insulators, Ltd. | Matrices pour la formation par extrusion d'un corps formé en nid d'abeille et procédé de formation du corps formé en nid d'abeille utilisant lesdites matrices |
| US9089992B2 (en) | 2007-04-30 | 2015-07-28 | Corning Incorporated | Methods and apparatus for making honeycomb structures with chamfered after-applied akin and honeycomb structures produced thereby |
| US20100052205A1 (en) * | 2008-08-27 | 2010-03-04 | Thomas William Brew | Method of forming ceramic honeycomb substrates |
| US8435025B2 (en) * | 2009-08-27 | 2013-05-07 | Corning Incorporated | Honeycomb extrusion die apparatus |
| US20110126973A1 (en) * | 2009-11-30 | 2011-06-02 | Andrewlavage Jr Edward Francis | Apparatus And Method For Manufacturing A Honeycomb Article |
| JP6196604B2 (ja) * | 2014-11-18 | 2017-09-13 | 日本碍子株式会社 | ハニカム成形体の押出成形用口金 |
| EP3414067B1 (fr) | 2016-02-11 | 2022-06-15 | Corning Incorporated | Composants d'extrusion de corps alvéolaires |
| WO2021108207A1 (fr) * | 2019-11-26 | 2021-06-03 | Corning Incorporated | Filière d'extrusion en nid d'abeilles pourvue d'un relief de gonflement |
Family Cites Families (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPS55140514A (en) * | 1979-04-21 | 1980-11-04 | Ngk Insulators Ltd | Preparation of mouth piece for extruding and molding honeycomb molding earth discharging foundation |
| JPS5838083B2 (ja) * | 1980-01-22 | 1983-08-20 | 株式会社日本自動車部品総合研究所 | ハニカム構造体押出成形用ダイス装置 |
| US4298328A (en) * | 1980-05-12 | 1981-11-03 | Corning Glass Works | Extrusion apparatus for preventing the distortion of peripheral cells in extruded honeycomb structures |
| JPS5777521A (en) * | 1980-10-31 | 1982-05-14 | Nippon Soken | Die device for molding honeycomb structure |
| JPS57157706A (en) * | 1981-03-25 | 1982-09-29 | Nippon Soken | Die for molding honeycomb |
| US5256054A (en) * | 1990-11-30 | 1993-10-26 | Corning Incorporated | Method and apparatus for forming a uniform skin on a cellular substrate |
| US5089203A (en) * | 1991-02-12 | 1992-02-18 | Corning Incorporated | Method and apparatus for forming an outer skin or honeycomb structures |
| JPH08169005A (ja) * | 1994-12-20 | 1996-07-02 | Babcock Hitachi Kk | ハニカム成形用口金およびハニカム成形体の製造方法 |
-
1998
- 1998-10-29 JP JP30880298A patent/JP3701801B2/ja not_active Expired - Fee Related
-
1999
- 1999-10-28 DE DE69919483T patent/DE69919483T2/de not_active Expired - Lifetime
- 1999-10-28 EP EP99308568A patent/EP0997247B1/fr not_active Expired - Lifetime
- 1999-10-29 US US09/429,631 patent/US6287103B1/en not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| JP3701801B2 (ja) | 2005-10-05 |
| US6287103B1 (en) | 2001-09-11 |
| JP2000127130A (ja) | 2000-05-09 |
| DE69919483T2 (de) | 2005-09-29 |
| DE69919483D1 (de) | 2004-09-23 |
| EP0997247A3 (fr) | 2002-05-29 |
| EP0997247A2 (fr) | 2000-05-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0997247A2 (fr) | Matrice d'extrusion pour la fabrication de corps en nid d'abeilles | |
| JP4159155B2 (ja) | セラミックハニカム構造体および押出金型 | |
| US5702659A (en) | Honeycomb extrusion die and methods | |
| US3905743A (en) | Extrusion apparatus for forming thin-walled honeycomb structures | |
| EP1594687B1 (fr) | Corps alveolaire ceramique et procede de fabrication | |
| CA1053446A (fr) | Methode et appareillage de fabrication d'ouvrages alveoles a parois minces | |
| US4550005A (en) | Extrusion die for ceramic honeycomb structure | |
| EP0570698B1 (fr) | Matrice d'extrusion en plusieurs parties | |
| US4178145A (en) | Extrusion die for ceramic honeycomb structures | |
| US10328627B2 (en) | Die assembly and method of extruding cellular ceramic substrates with a skin | |
| JPH02245313A (ja) | 厚い外皮を有するハニカム構造を成形するための押出ダイアセンブリ | |
| EP0275162B1 (fr) | Matrice d'extrusion pour structure en nid d'abeilles | |
| EP3414067B1 (fr) | Composants d'extrusion de corps alvéolaires | |
| CN108349110B (zh) | 用于蜂窝体的挤出模具 | |
| EP0997246B1 (fr) | Matrice d'extrusion pour la fabrication de corps en nid d'abeilles | |
| JPH0976219A (ja) | ハニカム構造体押出装置 | |
| EP0710514B1 (fr) | Extrusion de corps à structure en nid d'abeilles métallique | |
| EP0255043B1 (fr) | Filière d'extrusion pour des polymères thermoplastiques | |
| US12109727B2 (en) | Honeycomb extrusion dies and forming methods | |
| US7524448B2 (en) | Honeycomb extrusion die | |
| WO2022251010A1 (fr) | Filières d'extrusion en nid d'abeilles et leurs procédés d'utilisation et de fabrication | |
| JP2925893B2 (ja) | ハニカム構造体押出装置およびそれを使用したハニカム構造体の製造方法 | |
| JP4901345B2 (ja) | ボード体 | |
| JPS6341126Y2 (fr) | ||
| CN113681688B (zh) | 一种陶瓷膜挤出模具 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| RIC1 | Information provided on ipc code assigned before grant |
Free format text: 7B 28B 3/26 A, 7B 28B 3/20 B |
|
| 17P | Request for examination filed |
Effective date: 20020619 |
|
| AKX | Designation fees paid |
Designated state(s): BE DE FR GB |
|
| 17Q | First examination report despatched |
Effective date: 20030718 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): BE DE FR GB |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 69919483 Country of ref document: DE Date of ref document: 20040923 Kind code of ref document: P |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| ET | Fr: translation filed | ||
| 26N | No opposition filed |
Effective date: 20050519 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20051018 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20051025 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20051031 Year of fee payment: 7 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20061028 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20070629 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061028 |
|
| BERE | Be: lapsed |
Owner name: *NGK INSULATORS LTD Effective date: 20061031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20061031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20061031 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20181016 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 69919483 Country of ref document: DE |