EP1129867B1 - Verfahren und Vorrichtung zur Herstellung eines graphischen Produkts - Google Patents
Verfahren und Vorrichtung zur Herstellung eines graphischen Produkts Download PDFInfo
- Publication number
- EP1129867B1 EP1129867B1 EP00104347A EP00104347A EP1129867B1 EP 1129867 B1 EP1129867 B1 EP 1129867B1 EP 00104347 A EP00104347 A EP 00104347A EP 00104347 A EP00104347 A EP 00104347A EP 1129867 B1 EP1129867 B1 EP 1129867B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- layer
- graphic product
- sheet material
- web
- bonding
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims abstract description 49
- 238000004519 manufacturing process Methods 0.000 title claims description 29
- 239000000463 material Substances 0.000 claims abstract description 107
- 241000196324 Embryophyta Species 0.000 claims abstract description 87
- 239000000853 adhesive Substances 0.000 claims abstract description 59
- 230000001070 adhesive effect Effects 0.000 claims abstract description 59
- 238000010438 heat treatment Methods 0.000 claims abstract description 58
- 238000012546 transfer Methods 0.000 claims abstract description 31
- 239000003112 inhibitor Substances 0.000 claims abstract description 10
- 125000000391 vinyl group Chemical group [H]C([*])=C([H])[H] 0.000 claims description 66
- 229920002554 vinyl polymer Polymers 0.000 claims description 66
- 239000000758 substrate Substances 0.000 claims description 34
- 230000002093 peripheral effect Effects 0.000 claims description 19
- 238000005520 cutting process Methods 0.000 claims description 15
- 239000004820 Pressure-sensitive adhesive Substances 0.000 claims description 13
- 238000000926 separation method Methods 0.000 claims description 13
- 238000003860 storage Methods 0.000 claims description 7
- 239000011248 coating agent Substances 0.000 claims description 6
- 238000000576 coating method Methods 0.000 claims description 6
- 230000002401 inhibitory effect Effects 0.000 claims description 5
- 238000002844 melting Methods 0.000 claims description 5
- 230000008018 melting Effects 0.000 claims description 5
- 230000003213 activating effect Effects 0.000 claims description 4
- -1 polyethylene Polymers 0.000 claims description 4
- 238000003825 pressing Methods 0.000 claims description 4
- 239000004698 Polyethylene Substances 0.000 claims description 3
- 229920000728 polyester Polymers 0.000 claims description 3
- 229920000573 polyethylene Polymers 0.000 claims description 3
- 229920001296 polysiloxane Polymers 0.000 claims description 2
- 230000004044 response Effects 0.000 claims description 2
- 230000007246 mechanism Effects 0.000 abstract description 7
- 239000010410 layer Substances 0.000 description 90
- 230000008569 process Effects 0.000 description 13
- 238000007639 printing Methods 0.000 description 9
- 238000013461 design Methods 0.000 description 8
- 238000009333 weeding Methods 0.000 description 7
- 239000011888 foil Substances 0.000 description 5
- 239000002131 composite material Substances 0.000 description 4
- 230000003287 optical effect Effects 0.000 description 3
- 230000004913 activation Effects 0.000 description 2
- 239000012790 adhesive layer Substances 0.000 description 2
- 230000015572 biosynthetic process Effects 0.000 description 2
- 239000003795 chemical substances by application Substances 0.000 description 2
- 230000000295 complement effect Effects 0.000 description 2
- 238000010586 diagram Methods 0.000 description 2
- 238000005304 joining Methods 0.000 description 2
- 239000003094 microcapsule Substances 0.000 description 2
- 229920003023 plastic Polymers 0.000 description 2
- 239000004033 plastic Substances 0.000 description 2
- 229920001875 Ebonite Polymers 0.000 description 1
- 239000004743 Polypropylene Substances 0.000 description 1
- XUIMIQQOPSSXEZ-UHFFFAOYSA-N Silicon Chemical compound [Si] XUIMIQQOPSSXEZ-UHFFFAOYSA-N 0.000 description 1
- 239000004840 adhesive resin Substances 0.000 description 1
- 229920006223 adhesive resin Polymers 0.000 description 1
- 238000005452 bending Methods 0.000 description 1
- 239000000919 ceramic Substances 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 239000003086 colorant Substances 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 239000004519 grease Substances 0.000 description 1
- 239000000155 melt Substances 0.000 description 1
- 239000002184 metal Substances 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000013021 overheating Methods 0.000 description 1
- 229920006254 polymer film Polymers 0.000 description 1
- 229920001155 polypropylene Polymers 0.000 description 1
- 229920002635 polyurethane Polymers 0.000 description 1
- 239000004814 polyurethane Substances 0.000 description 1
- 238000012545 processing Methods 0.000 description 1
- 229910052710 silicon Inorganic materials 0.000 description 1
- 239000010703 silicon Substances 0.000 description 1
- 239000002210 silicon-based material Substances 0.000 description 1
- 239000002356 single layer Substances 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
- 238000006467 substitution reaction Methods 0.000 description 1
- 239000000725 suspension Substances 0.000 description 1
- 238000007651 thermal printing Methods 0.000 description 1
- 239000013598 vector Substances 0.000 description 1
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B44—DECORATIVE ARTS
- B44C—PRODUCING DECORATIVE EFFECTS; MOSAICS; TARSIA WORK; PAPERHANGING
- B44C1/00—Processes, not specifically provided for elsewhere, for producing decorative surface effects
- B44C1/16—Processes, not specifically provided for elsewhere, for producing decorative surface effects for applying transfer pictures or the like
- B44C1/165—Processes, not specifically provided for elsewhere, for producing decorative surface effects for applying transfer pictures or the like for decalcomanias; sheet material therefor
- B44C1/17—Dry transfer
- B44C1/1712—Decalcomanias applied under heat and pressure, e.g. provided with a heat activable adhesive
- B44C1/172—Decalcomanias provided with a layer being specially adapted to facilitate their release from a temporary carrier
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D7/00—Details of apparatus for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D7/27—Means for performing other operations combined with cutting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26F—PERFORATING; PUNCHING; CUTTING-OUT; STAMPING-OUT; SEVERING BY MEANS OTHER THAN CUTTING
- B26F1/00—Perforating; Punching; Cutting-out; Stamping-out; Apparatus therefor
- B26F1/38—Cutting-out; Stamping-out
- B26F1/3806—Cutting-out; Stamping-out wherein relative movements of tool head and work during cutting have a component tangential to the work surface
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B44—DECORATIVE ARTS
- B44C—PRODUCING DECORATIVE EFFECTS; MOSAICS; TARSIA WORK; PAPERHANGING
- B44C1/00—Processes, not specifically provided for elsewhere, for producing decorative surface effects
- B44C1/16—Processes, not specifically provided for elsewhere, for producing decorative surface effects for applying transfer pictures or the like
- B44C1/165—Processes, not specifically provided for elsewhere, for producing decorative surface effects for applying transfer pictures or the like for decalcomanias; sheet material therefor
- B44C1/17—Dry transfer
- B44C1/1712—Decalcomanias applied under heat and pressure, e.g. provided with a heat activable adhesive
- B44C1/1725—Decalcomanias applied under heat and pressure, e.g. provided with a heat activable adhesive using an intermediate support
Definitions
- This invention relates to a method for manufacturing graphic products such as designs or characters for signs and the like, and an apparatus for performing the method.
- the types of graphic products to which this invention is directed are characters or designs which adhere to a backing or substrate.
- the manufacturing of these types of graphic products generally involves the steps of cutting the graphic product from a layer of sheet material on a carrier sheet, removing the product from the carrier sheet and then attaching the product to the substrate.
- the present invention is directed to an automated method and apparatus for removing such graphic products from the carrier sheet and includes the selective removal of either the weed interlaced with the product or the graphic product itself.
- the invention also includes a unique heat activated bonding web for use with the method and apparatus.
- the sign making field includes apparatuses and methods for automated sign making, and includes automatic weeding systems and methods.
- U.S. Patent 5,143,576 issued on September 1, 1992 to Logan and owned by the assignee of the present invention discloses an apparatus and method for automating weed removal.
- the apparatus uses stored data in the form of vectors for attaching a bonding web comprising adhesive microcapsules to a graphic product or weed on a carrier sheet along a linear path offset from the periphery of the weed or graphic product.
- a pressure applicator tool activates the adhesive microcapsules within the web to temporarily bond the web to the graphic product or weed based on the stored data defining the periphery of the graphic product or weed.
- U.S. Patent No. 4,645,555 to Kuboyama discloses a hot stamping method used for the formation of sharp edged characters and/or numerals in a sheet material attached to a base plate for transfer from the base plate to a substrate. That is, raised numerals or characters are joined to a base plate, and a bonding web including a heat activated adhesive is pressed over the substrate and the numerals or letters. Upon heating the sheet material over its entire surface, the raised characters are joined to an adhesive comprising the sheet, and at the areas where no numerals exist the adhesive remains on the base plate. Therefore, heat is applied over the entire surface of the bonding web and base plate for adherence to the entire base plate surface including the surface of the numeral or character. Unlike the present invention, selective heating is not used for attaching the bonding web to the graphic product alone.
- U.S. Patent No. 4,374,691 to Vanden Bergh discloses a material and method for forming pressure transferable graphic designs.
- the invention includes a composite material and a method of forming characters or numerals in the composite material and removing the same therefrom for attachment to a substrate.
- the composite material includes a donor layer for supplying the letters or characters and an accepting layer for receiving the letters and characters.
- One step involves forming the letters and attaching the letters to the accepting layer.
- the letters are not preformed in a layer of sheet material on a carrier sheet as in the instant invention. Instead the letters are formed in a layer of sheet material on a carrier sheet by applying heat to the accepting sheet over the desired graphic design formation.
- the accepting sheet includes an adhesive which is activated upon heating, and during contact with the donor sheet, the adhesive causes sections of the donor sheet to attach to the accepting sheet in configurations resembling the graphic designs drawn.
- the donor sheet is comprised of a material which is easily fragmented and upon the application of the adhesive, sections matching the graphic designs adhere to the accepting layer.
- the graphic design may then be removed from the donor sheet and is pressure- or heat-transferred to a sign substrate.
- the patent to Vanden Bergh does not incorporate selective activation of a bonding web for registration with, and for joining to precut graphic products.
- U.S. Patent No. 5,112,423 to Liebe Jr. discloses a method of making and applying alignment maintaining plastic lettering material.
- the method in Liebe uses a composite sheet of material comprising an adhesive layer, a display layer and a release layer.
- the method includes cutting graphic letters or numerals and the like into the adhesive and display layer but not into the release layer, and stripping away the adhesive and display layers not within the desired outline of the numerals, letters or other graphic product. Accordingly, the release layer is left with the lettering thereon for transfer to a substrate.
- selective activation and attachment of a bonding web is not used for removing the symbols or letters from the release layer.
- U.S. Patent No. 4,933,124 to Duncun discloses a process for applying a silicon release coating to a polymer film.
- the Duncun process includes the application of a release film onto a substrate but the selective automated application of such a film to particular areas of the substrate using a selectively activated head is not disclosed.
- the invention also includes a laminated bonding web material having a heat sensitive adhesive and a friction reducing coating thereon for easing the advancement of the web across a heating head in practicing this invention.
- U.S. Patent No. 5,082,822 to Uytterhoeven et al. discloses a die donor element having a coating thereon for easing the passage of a sheet material under a thermal head during printing applications, such a material has not been uncovered with respect to selectively activated adhesive webs as disclosed herein.
- one object of this invention is to provide a highly accurate method and apparatus for automated removal of characters and other graphic products or the weed associated therewith from a carrier sheet by selectively attaching a bonding web for convenient transfer of the product to a sign substrate.
- a further object of this invention is to provide a method and apparatus for accomplishing automated weeding and graphic product removal without risk of tearing the graphic products.
- a still further object of this invention is to provide an automatic weeding and graphic product transfer apparatus and method that are compatible with and complementary to existing successfully marketed sign manufacturing equipment.
- the present invention resides in a method and apparatus for manufacturing a graphic product from a layer of sheet material releasably secured to a carrier sheet for subsequent transfer of the graphic product to a substrate.
- one portion of the layer of sheet material defines the graphic product and is severed from the remaining portions of the layer of sheet material along lines of cut at the peripheral edges of the graphic product.
- the present invention is directed to an automated method and apparatus for selectively securing a bonding web to the portions representing the graphic product or weed associated therewith wherein the portions selectively secured are defined by data in a microprocessor which controls the apparatus.
- the invention provides an apparatus according to claim 1, and methods according to claims 11 and 22. Embodiments of the invention are defined in the dependent claims.
- the method of this invention includes placing a bonding web in overlying relationship with a layer of sheet material with a heat activated adhesive between the bonding web and the layer of sheet material.
- the bonding web is selectively heated over at least one application area which substantially registers with an underlying one of the portions of the layer of sheet material to activate the adhesive and attach the bonding web to the one of the sheet material portions. Thereafter, the bonding web is pulled to remove the attached portion from the carrier sheet.
- the attached portion may be either the graphic product portion or the weed portion.
- An apparatus for carrying out this method includes storage means for storing data defining the peripheral edges of a graphic product as machine readable data.
- Feeding means feed the layer of sheet material releasably secured to the carrier sheet and a bonding web having a heat activated adhesive adjacent one side through the apparatus in an overlying relationship adjacent a heating means to activate the adhesive.
- the heating means is comprised of a plurality of elements positioned in contact with the bonding web and adjacent the layer of sheet material for activating the adhesive.
- Control means interfaced with the storage means and connected to the heating means causes the elements to be selectively energized in response to the stored data.
- the elements activate the adhesive in an application area registering with one of the portions of the layer of sheet material while the feeding means feeds the bonding web and layer of sheet material on the carrier sheet relative to the heating means. Accordingly, the bonding web becomes attached to one portion or the other of the layer of sheet material.
- the storage means is a computer memory which stores the peripheral edges of a graphic product as machine readable data which is downloaded to the control means for selectively activating the heating elements arranged linearly in a thermal head of the heating means.
- the heating elements attach the bonding web to the sheet material on the carrier sheet when the sheet material is moved past the thermal head by the feeding means.
- an adhesive inhibitor can be applied to an application area for subsequent removal of the remaining material via an adhesive transfer web.
- the feeding means in one embodiment incorporates belt driven sprockets and a roller platen.
- the sprockets have pins extending from the peripheries thereof for engaging feed holes extending adjacent the longitudinal edges of the carrier sheet.
- the sprockets and roller platen move the layer of sheet material, carrier sheet and the overlying bonding web adjacent the heating elements of the thermal head.
- the adhesive is activated and the bonding web attaches substantially exclusively to either the graphic product or weed material to be removed from the carrier sheet. If the portion first removed from the carrier sheet is the weed, the remaining portion of the layer of sheet material on the carrier sheet is run through the apparatus a second time, and a second bonding web is selectively attached to the remaining weed or the graphic product on the carrier sheet. When bonding is complete, the bonding web together with the attached weed or product is separated from the carrier sheet. The bonding web or an adhesive transfer web attached to the graphic product is used to transfer the graphic product to a graphic product substrate.
- the layer of sheet material attached to the carrier sheet and the bonding web are supplied by the feed means from separate rolls rotatably mounted on the apparatus.
- weed or graphic products used for making signs can be removed from a carrier sheet via an automated apparatus and method.
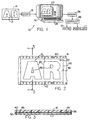
- Fig. 1 is a schematic diagram illustrating a system for cutting a graphic product in a layer of sheet material on a carrier sheet and separating the product from the carrier sheet in accordance with the present invention.
- Fig. 2 is a fragmentary view of a graphic product cut in a layer of sheet material on a carrier sheet having feed holes extending longitudinally along each edge.
- Fig. 3 is an enlarged cross-sectional view of the sheet material on the carrier sheet as viewed along line 3-3 of Fig. 2.
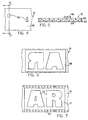
- Fig. 4 is a fragmentary view of a bonding web with internal weed attached thereto after weeding the graphic product in Fig. 2.
- Fig. 5 is an enlarged cross-sectional view of the bonding web taken along line 5-5 of Fig. 4.
- Fig. 6 is a fragmentary view of another bonding web with external weed attached thereto after weeding the product in Fig. 2.
- Fig. 7 is a fragmentary view of a graphic product on the carrier sheet after all the weed has been removed from the carrier sheet.
- Fig. 8 is a fragmentary view of still another bonding web used in a graphic product transfer process with the graphic product attached thereto.
- Fig. 9 is a perspective view of a bonding apparatus used in the system of Fig. 1.
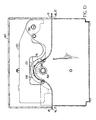
- Fig. 10 is a side elevation view of the interior of the bonding apparatus.
- Fig. 11 is an enlarged fragmentary view of the bonding apparatus in Fig. 10 and shows a feed mechanism for moving the bonding web and layer of sheet material on a carrier sheet through the bonding apparatus.
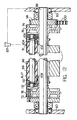
- Fig. 12 is a fragmentary front view showing a support structure and drive mechanism for a roller platen and drive sprockets in the bonding apparatus.
- Fig. 13 is another side elevation view showing an open and closed position of the upper frame of the bonding apparatus.
- Fig. 14 is an enlarged fragmentary view of the apparatus, similar to Fig. 11, and shows the thermal head, roller platen and drive sprockets.
- Fig. 15 is a schematic diagram of a combined cutting, bonding and separating process in accordance with the present invention.
- Fig. 16 is a fragmentary sectional view of the process in Fig. 15 for separating a bonding web having an attached weed portion or graphic product from a carrier sheet.
- Fig. 1 illustrates a microprocessor controlled system, generally designated 10, which controls a bonding apparatus 11 as well as a cutter 12 to manufacture a graphic product in accordance with the present invention.
- the cutter 12 cuts a graphic product, such as the letters "AR" of a sign or logo from a layer of sheet material releasably secured to a carrier sheet.
- the bonding apparatus 11 Based on data 14 input into the system, the bonding apparatus 11 selectively bonds a bonding web to a designated portion of the cut layer of sheet material for subsequent separation and removal of the portion from the carrier sheet.
- the system 10 includes a digitizer 18 for converting graphic data 14 into machine readable data for storage and use by a microprocessor-based computer 19.
- the machine readable data includes parameters defining the interior and exterior peripheral edges 20 of the graphic product 13 as shown in Fig. 2.
- the data defining the peripheral edges is displayed on a monitor 22 in the form of a graphic image.
- the graphic image may be altered by inputting further information into the computer 19 through a keyboard 24 or the like.
- a printing process may be included as a step prior to cutting.
- an enhancement program may be included in the system so as to change the graphic image through the printing of shading, halftones and colors as described in greater detail in U.S. Patent No. 5,537,135 and having the same assignee.
- the system is open to a variety of different software programs and the like for altering the graphic images manufactured.
- An operating program in the computer 19 interprets the machine readable data and runs a variety of operations from the computer, including the operation of the cutter 12, and the bonding apparatus 11.
- the computer 19 generates cutting, bonding and possibly printing programs from the machine readable data, and the programs are stored in a memory 26 and read by the controller 28 of Fig. 1.
- the controller 28 operates both the cutter 12 and the bonding apparatus 11, and if desired, a printer, based on the graphic data 14 input into the system 10.
- a suitable cutter 12 for carrying out the cutting operation is described in U.S. Patents 4,467,525; 4,799,172 and 4,834,276, all owned by the assignee of the present application.
- the cutter cuts a path defining the peripheral edges 20 of the graphic product 13 in a layer of sheet material 16 which is releasably secured to a carrier sheet 17 as shown in Figs. 2 and 3.
- the layer of sheet material 16 is preferably formed from vinyl and the carrier sheet 17, which is not cut, is formed from heavy paper or tag board.
- the vinyl layer 16 is releasably attached to the carrier sheet 17 via a pressure sensitive adhesive 38.
- the carrier sheet 17 is coated with a release agent 32 so that only a temporary bond holds the vinyl layer 16 on the carrier sheet 17.
- the vinyl layer 16 in one form is HP220 Scotchcal vinyl sheet manufactured by the 3M Corporation.
- the strip formed by the vinyl layer and the carrier sheet has a row of feed holes 40 extending along each longitudinal edge of the strip for feeding the strip through the cutter 12 and bonding apparatus 11 of Fig. 1
- the material is divided into two portions, the graphic product 13 and the weed.
- the graphic product 13 consists of the letters "AR" and the weed is the remainder including the internal weed 46 defined by the internal peripheries or edges of the graphic product, and the external weed 48 outside the external peripheries of the graphic product.
- a border 49 may be cut around the graphic product to define the outer limit of the external weed 48 and to ease removal of the external weed from the carrier sheet 17. The cut border is advantageous, but not required.
- a registration circle 51 is also cut into the layer of sheet material 16 as shown in Fig. 2.
- the circle 51 is cut adjacent one of the feed holes 40 along the longitudinal edges of the strip and is used to identify and properly locate the origin of the graphic product in the bonding apparatus 11 after it emerges from the cutter 12.
- the bonding apparatus 11 of Fig. 1 selectively attaches a bonding web by means of a heat activated adhesive to the cut portions of the vinyl layer 16.
- a bonding web 15 is first attached to the internal weed 46, and the weed is removed from the carrier sheet by pulling the bonding web 15 and the carrier sheet apart with the internal weed clinging to the bonding web as shown in Fig. 4.
- another bonding web 15 is attached to the external weed 48 and the external weed is removed from the carrier sheet by the bonding web as shown in Fig. 6.
- the graphic product 13 "AR" remains alone on the carrier sheet 17 within the border as shown in Fig.
- the product is suitably shaped and weed portions 46,48 are large enough, it is possible to omit the steps of removing the weed, and to attach a bonding web initially to the product 13 for removal from the carrier sheet in a single step.
- a two step process is used in which the internal weed is first removed from the carrier sheet with a first bonding strip, and the graphic product is then removed with a second bonding strip to leave the external weed on the carrier sheet.
- a bonding web 15 with the adhesive forming an integral part thereof, as shown in Figs. 4 and 5, is comprised of two layers of material.
- a first layer 52 is formed from a biaxially oriented polyester having a melting temperature of approximately 300° F.
- the layer is coated with a friction-reducing material 54 to ease advancement of the bonding web adjacent heating elements in the bonding apparatus 11 as described below.
- the material 54 may be a silicon based material.
- a second layer 56 of the web 15 is secured to the first layer 52 and is comprised of polyethylene, polypropylene or a polyurethane or other similar material having a melting temperature of approximately 225° F to form a high tack releasable adhesive upon heating.
- the first layer 52 maintains its structural integrity while the second layer 56 melts and forms an adhesive to attach the web 15 to a selected portion of the cut vinyl layer 16.
- a single layer of polyester can be coated with a heat activated dry adhesive for attaching the bonding web to the weed or product portions, or a heat activated adhesive can be interposed between the sheet material and web in a separate step.
- the bonding apparatus 11 has an outer shell or housing 60 to which the components of the bonding apparatus are attached.
- the housing is comprised of a hinged cover 61 which has a handle 62 for assisting in opening the cover to expose the internal mechanism.
- Rolls 64,66 may be used for supplying the strip consisting of the now-cut vinyl layer 16 on the carrier sheet 17 and the bonding web 15, respectively, into the bonding apparatus, and are rotatably mounted in a rack 68 at the rear of the apparatus.
- the strip and the bonding web 15 are fed from the separate rolls over a dancer roller 69 into the bonding apparatus 11 in overlying relationship, and exit the bonding apparatus 11 at the front side of the machine as shown in Fig. 9. They may be retrieved as desired including, for example, manual retrieval or retrieval via take-up rolls.
- the web may be manually supplied by opening the cover 61 and placing the web in an overlying manner on the vinyl layer 16. With this alternative, however, the layer is preferably still fed from the roll 64.
- the bonding apparatus is automatically controlled from the controller 28, the bonding apparatus also has an additional control panel 70 accessible from outside of the apparatus as shown in Fig. 9 to allow an operator to manually control the feeding and bonding operation.
- the bonding apparatus has a feed mechanism for advancing the strip of cut vinyl material on the carrier sheet 17 and the bonding web 15 through the bonding apparatus relative to a thermal head 101 which bonds the web 15 selectively to the vinyl layer 16.
- the feed mechanism includes two driven sprockets 72,74 having a plurality of equally spaced pins 76 extending from and around the periphery of the sprockets, as shown most clearly in Figs. 10 and 12.
- the pins engage the rows of feed holes 40 extending along both longitudinal edges of the strip.
- the drive sprockets 72,74 are fixedly mounted to a drive shaft 88, which is rotatably mounted within the housing 60 of the bonding apparatus and driven by a stepmotor 90 shown in Fig. 11 through a series of drive gears 92,94, two drive pulleys 96,98 and a toothed drive belt 100.
- a roller platen 99 is also rotatably mounted within the housing 60 and is driven from the drive shaft 88 by means of drive pulleys 102,104 and an O-ring drive belt 106 at one end of the platen and drive pulleys 108,110 and an O-ring drive belt 112 at the opposite end of the platen.
- the gears, toothed drive belt and sprockets insure that the bonding web 15 and vinyl layer 16 on the carrier sheet 17 are precisely positioned on the roller platen 99 under the thermal head 101. In addition, they control the speed at which the vinyl layer 16 on the carrier sheet 17 and bonding web 15 move through the bonding apparatus.
- the drive pulleys 102,104,108,110 are selected to establish a peripheral speed of the roller platen 99 that is slightly higher than the peripheral speed of the drive sprockets 72,74 to assist the feeding of the vinyl layer 16 on the carrier sheet and the bonding web 15 past the thermal head 101 shown in Figs. 10 and 14. Since the drive sprockets 72,74 positively engage the layer of sheet material 16 on the carrier sheet 17 and control the speed of the sheet, the O-ring drive belts 106,112 must allow limited slip to prevent tearing.
- a pair of curved, sheet metal plates 114,116 guide the bonding web 15 and the vinyl layer 16 on the carrier sheet 17 circumaxially onto and off of the roller platen 99 and each of the cylindrical support surfaces of the sprockets 72,74 in a U-shaped feed path.
- the cylindrical surfaces of the sprockets lie in a cylindrical plane much larger in diameter than the cylindrical, strip-engaging surface of the roller platen 99 which is tangential to the cylindrical plane.
- the cylindrical surface of the roller platen 99 is formed by a hard rubber sleeve which improves the frictional engagement of the platen with the carrier sheet 17.
- a pair of holddown bales 118 (only one shown) support two holddown wipers 124, 126 at the supply and discharge points of the sprockets.
- the bales are pivotally suspended from the housing 60 on pins 120 as indicated in Fig. 13, so that the bails and wipers can be lifted away from the sprockets and allow the bonding web 15 and vinyl layer 16 on the carrier sheet 17 to be mounted on and removed from the sprockets and roller platen 99.
- Overcenter springs 122 are connected to the housing adjacent the pivotal ends of the holddown bales and assist in holding the wipers down on the vinyl layer 16 on the carrier sheet 17 and bonding web 15.
- an optical sight 127 supported from the housing 60 of the bonding apparatus can be temporarily swiveled over the roller platen 99 to accurately locate the origin circle 51 (Fig. 2) of the graphic product cut into the vinyl layer 16 and bring that origin into registration with the origin of the corresponding bonding program controlling the operation of the bonding apparatus 11.
- the cutting program which guides the cutter 12 (Fig. 1) and the bonding program which operates the bonding apparatus 11 use the same data defining the peripheral edges of the graphic product 13 so that the bonding web 15 is accurately bonded to either the weed or the graphic product created by the cutting program. Correlation of the cutting and bonding programs on the material is brought about by starting both operations at the registration circle 51 or origin in the vinyl layer.
- the vinyl layer 16 and underlying carrier sheet are first positioned on the sprockets 72,74 and the sprockets are slewed by the operator of the bonding apparatus until the registration circle 51 is centered in the optical sight 127.
- the temporary position of the optical sight is in a vertical plane directly above the center of the roller platen 99 at a known position offset from the sprocket pins 76.
- Figure 14 illustrates the layer of sheet material 16 on the carrier sheet 17 and bonding web 15 passing over the roller platen 99 relative to and adjacent the thermal head 101.
- the thermal head is similar to thermal printing heads used in printing operations such as that disclosed in U.S. Patent No. 5,537,135 and owned by the Assignee of this application. However, unlike printing heads, no printing ribbon or web is used with the thermal head 101 in this invention.
- the thermal head 101 has a plurality of heating elements distributed evenly along the head from one end of the roller platen 99 to the other and the heating elements are densely packed along a line of contact with the head, preferably with a density of 300 elements per inch.
- One such head is made by Kyocera Industrial Ceramics Incorporated of Kyocera, Japan.
- the elements can be energized individually to selectively activate the heat-activated adhesive layer of the bonding web 15 and thereby attach the web to the weed or graphic product portion of the vinyl layer 16.
- the thermal head 101 is mounted in the upper support frame 130 pivotally supported in the housing 60 by a shaft 132.
- a suspension plate 134 is connected with the frame 130 by means of a series of bolts 136 which are secured to the plate 134 and slidably received within the frame 130 so the plate 134 together with the thermal head 101 can move vertically relative to the support frame.
- the mounting plate 134 also serves as a heat sink for the heat generated in the thermal head.
- Surrounding each of the sliding bolts 136 and interposed between the frame 130 and plate 134 are several coil springs 138 which, with the support frame lowered and latched in the closed position as shown in Figs. 10 and 14, apply pressure downwardly on the plate 134 and press the thermal head 101 against the bonding web 15 and vinyl layer 16 on the carrier sheet 17 and the roller platen 99 along a line of contact extending horizontally at the roller platen.
- the bonding and separating operations can proceed.
- the cut vinyl layer 16 on the carrier sheet 17 and bonding web 15 are fed in overlying relationship over the roller platen and under the thermal head, as shown in Fig.14.
- the heating elements of the thermal head 101 are energized in a pattern substantially registering with either the graphic product portion or weed portion cut into the vinyl layer 16.
- either of the portions can be selected for bonding to the web 15 and subsequent removal from the carrier sheet 17. Accordingly, if the internal weed 46 shown in Fig. 2 is selected for removal, the heating elements are selectively energized at different parts of the thermal head 101 at selected times and for given durations as the web 15 and vinyl layer 16 move under the head to attach the web to the vinyl in an application area or pattern registering in position and shape with all or substantially all of the internal weed.
- the heating elements may be energized over the weed in solid pattern or in other patterns matching the shape of the weed.
- the elements and the adhesive of the bonding web can be activated in a plurality of discrete, evenly spaced zones, such as in a striped or checkered board pattern which terminates at the edges of the weed portion and covers the entire portion.
- the bonding web 15 is heated over an application area matching the patterns cut in the vinyl, i.e. the shape of the internal weed or sections of internal weed designated for removal from the carrier sheet, and the adhesive formed by the bottom layer of the bonding web is activated in a pattern and attaches the web to the internal weed.
- the thermal head also heats the pressure sensitive adhesive between the vinyl and the carrier sheet to assist in loosening the attached portions from the carrier sheet 17.
- Fig. 4 is indicative of the results of separation, and shows the internal weed 46 attached to the bonding web 15.
- the external weed 48 (Fig. 2) is removed from the carrier sheet 17 by passing the cut vinyl layer 16 on the carrier sheet through the bonding apparatus 11 a second time with a second bonding web 15.
- the process of external weed removal is similar to that described above for the internal weed except that the heating elements are energized over an application area or pattern substantially registering in position and shape with the external weed 48.
- the second bonding web and attached weed are then separated from the carrier sheet and appear as shown in Fig. 6.
- the only portion of the vinyl layer 16 left on the carrier sheet 17 within the frame is the graphic product 13 as shown in Fig. 7.
- the graphic product can now be removed in the same manner as the weed portions by processing the vinyl layer and carrier sheet with a third bonding web through the bonding apparatus 11, and energizing the thermal head to heat the bonding web in a pattern corresponding to the product. The product is then lifted from the carrier sheet and is transferred on the bonding web to a sign substrate for attachment.
- the graphic product can be transferred to a sign substrate by pressing an adhesive transfer web against the product to establish a temporary bond for stripping the product from the carrier sheet. This process is described in U.S. Patent 4,467,525.
- the pressure sensitive adhesive joining the vinyl to the carrier sheet stays with the graphic product during stripping due to the release coating on the carrier sheet. Since the pressure sensitive adhesive establishes a stronger bond with a sign substrate than the temporary bond with the transfer or bonding web, the adhesive will secure the graphic product to the substrate and allow the web to be stripped away.
- the external weed does not have to be removed from the carrier sheet before the graphic product.
- the cut vinyl layer 16 on the carrier sheet 17 and an overlying bonding web can be processed through the bonding apparatus 11 as described immediately above to join the product to the bonding web without first removing any of the weed.
- the graphic product portion is designated for removal via the keyboard 24 in Fig. 1.
- the controller 28 causes the heating elements of the thermal head to energize and activate the heat-activated adhesive of the web in an application area corresponding in position and shape with the graphic product.
- the bonds formed by the various combinations of materials and adhesives must necessarily be stronger or weaker relative to each other.
- the strength of the temporary bond between the carrier sheet 17 and graphic product 13 in the vinyl layer 16 must be less than the strength of the bond formed between the bonding web 15 and the graphic product so as to accomplish the separation of the graphic product from the carrier sheet 17.
- These same relative strengths are also necessary for the separation of the weed portion from the carrier sheet.
- the resulting bond by the pressure sensitive adhesive must be stronger than the bond formed between the bonding web 15 and the graphic product. That is, the pressure sensitive adhesive 38 must form a bond with the non release coated substrate stronger than the bond between the graphic product and the bonding web 15.
- Table 1 indicates that when the graphic product portion or weed portion of the layer 16 consisting of HP220 Scotchcal vinyl is joined with the polyethylene of the bonding web 15 by the thermal head 101 as discussed above, a bond having an adhesive strength of 3.11 N/cm (1.75 lb./in) is exhibited. This strength has been found to be highly effective in overcoming the temporary bond between the HP220 Scotchcal vinyl and the carrier sheet of approximately 2,67 N/cm (1.5 lb./in) or less.
- This 2,67 N/cm (1.5 lb./in.) bond is weak enough to allow the 3,11 N/cm (1.75 lb./in.) bond between the graphic product or weed and the bonding web 15 to be maintained during stripping from the carrier sheet.
- the bond strength between a non-release coated plastic, when used for the sign substrate 50, and the HP220 Scotchcal vinyl portions coated with the pressure sensitive adhesive is 4,305 N/cm (2.42 lb./in.). This bond is strong enough to overcome the 3.11 N/cm (1.75 lb./in.) bond between the graphic product and the bonding web, and thus permits separation of the vinyl material from the bonding web.
- the entire sign making process including weeding can be performed continuously in a fully automatic, integrated system as illustrated in Fig. 15.
- the system has four stages: a cutting stage I, a bonding stage II, a bonding stage III and a transfer stage IV.
- stage I the cutter 12 cuts the graphic product in the vinyl layer 16 on the carrier sheet 17 as previously described.
- the cut vinyl layer on the carrier sheet is processed from the output of the cutter directly to the input of a first bonding apparatus 11 in stage II where a first bonding web 15 from supply spool 66a is overlaid on the cut vinyl for selective attachment, for example, to the internal weed.
- the bonding web with attached weed is stripped from the rest of the cut vinyl by a take-up spool 140, and the carrier sheet with the remaining vinyl is processed directly to the input of a second bonding apparatus 11 in stage III by means of feed sprockets 142.
- stage III another bonding web 15 from a supply spool 66b is overlaid on the cut vinyl for selective attachment, for example, to the external weed.
- the bonding web with the attached weed is stripped from the rest of the vinyl by a take-up spool 144, and the carrier sheet and now-weeded graphic product are processed directly to the input of a transfer device in stage IV by the feed sprockets 146.
- a transfer web 150 from spool 148 lifts the graphic product from the carrier sheet which is reeled onto a take-up spool 152 while the graphic product is transferred by the transfer web 150 to a sign substrate 50 where a press 154 applies the graphic product to the substrate to produce the finished sign.
- the transfer sheet 150 is taken up on spool 156.
- the most effective method of separation is by pulling the web from the carrier at an angle of 120° as shown in Fig. 16.
- a backing plate 168 adjacent the inside radius formed by the bending of the bonding web, as shown in Fig. 16 good release and separation may be obtained.
- the plate 168 allows a small radius to be maintained at the bend point of the bonding web during the separation process and assists as well as in maintaining a constant pressure on the web.
- the bonding apparatus 11 can also be employed in a further weeding operation in which a heat-activated release material or adhesive inhibitor is transferred from a carrier web onto the cut vinyl layer 16 in a selected pattern corresponding to the weed.
- a supply web bearing a heat-releasable silicone or grease is overlaid on the cut vinyl layer 16 and the carrier sheet 17, and the materials so laminated are fed through the bonding apparatus in the same manner as the bonding web overlaid on the cut vinyl layer.
- the key board 24 in Fig. 1 calls up the pattern corresponding to the weed to energize the thermal head and cause the heat-activated adhesive inhibitor to be released from the supply web and be deposited on the weed portion only of the vinyl.
- the supply web is removed from the vinyl and a transfer sheet with pressure sensitive adhesive is applied to the graphic product portion of the vinyl to strip the graphic product from the carrier sheet and the remaining vinyl on the sheet.
- the adhesive inhibitor overlying the weed portion of the vinyl prevents the transfer web from adhering and, thus, permits the graphic product to be lifted away from the carrier sheet for transfer to a sign substrate.
- the inhibiting web may be supplied in cassette format.
- the description of the cassette format is incorporated herein by reference to Patent No. 5,537,135 and owned by the Assignee of the present invention.
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Forests & Forestry (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Lining Or Joining Of Plastics Or The Like (AREA)
- Electrical Discharge Machining, Electrochemical Machining, And Combined Machining (AREA)
- Heating, Cooling, Or Curing Plastics Or The Like In General (AREA)
- Making Paper Articles (AREA)
- Decoration By Transfer Pictures (AREA)
Claims (22)
- Vorrichtung zur Herstellung eines graphischen Produkts (13) aus einer Blattmaterialschicht (16), die lösbar an einer Trägerschicht (17) befestigt ist, wobei ein Bereich der Blattmaterialschicht das graphische Produkt (13) definiert, das von den verbleibenden Bereichen (46, 48) der Blattmaterialschicht auf der Trägerschicht entlang Schnittlinien an den Umfangskanten (20) des graphischen Produkts abgetrennt wird, und wobei die Vorrichtung umfaßt:a) Speichermittel (26) zum Speichern von Daten, welche die Umfangskanten (20) des graphischen Produkts (13) definieren, als maschinenlesbare Daten;b) eine haftende Bahn (15), die auf einer Seite der Bahn mit einem hitzeaktivierbaren Klebemittel wirkt;c) Transportmittel (72, 74, 90) zum Transportieren der lösbar an der Trägerschicht befestigten Blattmaterialschicht und der haftenden Bahn durch die Vorrichtung, wobei die eine Seite der Bahn, welche das Klebemittel trägt, an der Blattmaterialschicht anliegt;d) ein Hitzemittel (101) mit mehreren selektiv anregbare Hitzeelementen, das relativ zu den Transportmitteln derart angeordnet ist, daß die Hitzeelemente die an der Blattmaterialschicht anliegende haftende Bahn berühren; unde) Steuermittel (28), die mit den Speichermitteln (26) eine Schnittstelle haben und mit den Transportmitteln und dem Hitzemittel (101) verbunden sind, um zu bewirken, daß die Hitzeelemente als Reaktion auf die gespeicherten Daten selektiv angeregt werden, um das Klebemittel auf der haftenden Bahn gemäß einem im wesentlichen kontinuierlichen Muster entsprechend einem der Bereiche der Blattmaterialschicht zu aktivieren, während die Transportmittel die haftende Bahn und die lösbar an der Trägerschicht befestigte Blattmaterialschicht relativ zu dem Hitzemittel transportieren, um die Bahn mit dem einen der Bereiche des Blattmaterials zu verbinden.
- Vorrichtung zum Herstellen eines graphischen Produkts nach Anspruch 1, wobei die haftende Bahn (15) umfaßt:a) eine erste aus Polyestermaterial gebildete Schicht, die eine erste Schmelztemperatur hat;b) eine zweite aus einem reibungsreduzierenden Material gebildete zweite Schicht (54), welche die erste Schicht bedeckt, um das Vorrücken der haftenden Bahn, die an dem Hitzemittel anliegt, zu erleichtern; undc) daß die hitzeaktivierte Schicht (56) eine dritte Schicht ist, die aus Polyethylen gebildet ist und an der ersten Schicht (52) haftet und eine geringere Schmelztemperatur hat als die erste Schicht.
- Vorrichtung zum Herstellen eines graphischen Produkts nach Anspruch 2, wobei das reibungsreduzierende Material aus einem Silikonmaterial gebildet ist.
- Vorrichtung zum Herstellen eines graphischen Produkts nach den Ansprüchen 1, 2 oder 3, wobei das Transportmittel zwei Transportrollen (72, 74) mit Transportstiften (76) hat, wobei die Transportstifte von den Transportrollen abstehen, um mit Transportlöchern (40) in der lösbar an einer Trägerschicht (17) befestigten Blattmaterialschicht (16) in Eingriff zu kommen.
- Vorrichtung zum Herstellen eines graphischen Produkts nach Anspruch 4, die ferner eine datengesteuerte Schneidvorrichtung (12) hat, die mit dem Speichermittel (26) verbunden ist und auch auf die gespeicherten Daten reagiert, welche die Umfangskanten (20) des graphischen Produkts definieren, um die Schneidlinien zu erzeugen, die den Umfang eines graphischen Produkts sowie die Bereiche (13, 46, 48) definieren, wobei die Schneidvorrichtung (12) auch Transportmittel in Form von Transportrollen mit Transportstiften umfaßt, die mit den Transportlöchern in Eingriff kommen und die lösbar an einer Trägerschicht befestigte Blattmaterialschicht transportieren.
- Vorrichtung zum Herstellen eines graphischen Produkts nach Anspruch 5, ferner umfassend:a) Führungsmittel, die zwischen der Schneidvorrichtung (12) und dem Hitzemittel (101) angeordnet sind, um die lösbar mit der Trägerschicht (17) verbundene geschnittene Blattmaterialschicht (16) von der Schneidvorrichtung zu dem Hitzemittel zu transportieren; undb) Zufuhrmittel (66a, 66b) zum Leiten der haftenden Bahn (15) auf die lösbar einer Trägerschicht befestigte Blattmaterialschicht (16) auf den Führungsmitteln zwischen der Schneidvorrichtung und dem Hitzemittel.
- Vorrichtung zum Herstellen eines graphischen Produkts nach einem der vorhergehenden Ansprüche, ferner umfassend;
Zufuhrmittel (64, 66) zum Halten einer Menge des lösbar an der Trägerschicht (17) befestigten Blattmaterials und der haftenden Bahn (15); und
Abgabemittel (69) zum gemeinsamen Zuführen des Blattmaterials (16), das lösbar der Trägerschicht befestigt ist, und der haftenden Bahn an die Transportmittel (72, 74, 90). - Vorrichtung zum Herstellen eines graphischen Produkts nach einem der Ansprüche 4 bis 7, wobei die Transportmittel ferner umfassen:a) eine Auflagerolle (99), die um eine zentrale Achse drehbar ist und eine glatte Auflagefläche hat, welche die haftende Bahn (15) und die Blattmaterialschicht (16) derart auf der Trägerschicht (17) trägt, daß sie an Hitzeelementen des Hitzemittels (101) anliegen, wobei die Auflagerolle mit der Trägerschicht reibschlüssig in Eingriff ist und die lösbar an der Trägerschicht befestigte Materialschicht und die haftende Schicht anliegend an dem Hitzemittel (101) trägt; undb) eine Antriebsvorrichtung (90), die derart mit den Transportrollen (72, 74) und der Auflagerolle (99) verbunden ist, daß sie die Transportrollen und die Auflagerolle dreht, um die an der Trägerschicht befestigte Blattmaterialschicht und die haftende Bahn an den Hitzeelemente vorbei zu bewegen.
- Vorrichtung nach Anspruch 8, wobei die Antriebsvorrichtung (90) die Auflagerolle (99) mit einer leicht schnelleren Umfangsgeschwindigkeit als die Transportrollen dreht.
- Vorrichtung zum Herstellen eines graphischen Produkts nach einem der vorhergehenden Ansprüche, ferner umfassend ein druckerzeugendes Mittel (138) zum Pressen des Hitzemittels gegen die lösbar an einer Trägerschicht befestigte Blattmaterialschicht und die haftende Bahn, um dazu beizutragen, daß sich die haftende Bahn mit einem der Bereiche verbindet.
- Verfahren zum Herstellen eines graphischen Produkts, umfassend die folgenden Schritte:a) zur Verfügung Stellen einer Blattmaterialschicht (16) auf einer Trägerschicht (17), wobei ein Bereich der Blattmaterialschicht ein graphisches Produkt (13) definiert, das von einem anderen Bereich (46, 48) der Schicht des Blattmaterials, das den Ausschuß bildet, entlang Schnittlinien an den Umfangskanten (20) des graphischen Produkts abgetrennt wird;b) Plazieren einer haftenden Bahn (15) derart, daß es die Blattmaterialschicht (16) überdeckt, wobei zwischen der haftenden Bahn und der Blattmaterialschicht ein hitzeaktiviertes Klebemittel (56) angeordnet ist; undc) selektives Erhitzen der haftenden Bahn (15) mittels selektiv anregbarer Hitzeelemente über mindestens eine Auftragefläche, die im wesentlichen einem darunterliegenden Bereich der Bereiche der Blattmaterialschicht (16) entspricht, zum Aktivieren des Klebemittels am Umfang und innerhalb des Umfangs des einen Bereichs der Bereiche und Verbinden der haftenden Bahn (15) mit dem im wesentlichen gesamten einen Bereich (13 oder 46, 48) der Bereiche; undd) Abtrennen der haftenden Bahn (15) zusammen mit dem einen Bereich (13 oder 46, 48) der Bereiche, der daran befestigt ist, von dem anderen Bereich der Blattmaterialschicht und der Trägerschicht (17), um das graphische Produkt (13) von dem Ausschuß (46, 48) zu trennen.
- Verfahren zum Herstellen eines graphischen Produkts nach Anspruch 11, ferner umfassend die folgenden Schritte:c1) Pressen der haftenden Bahn (15) gegen die Blattmaterialschicht (16) während des Schrittes des Erhitzens zum selektiven Verbinden der Auftragefläche der haftenden Bahn mit dem im wesentlichen gesamten einen Bereich (13 oder 46, 48) der Bereiche.
- Verfahren zum Herstellen eines graphischen Produkts nach den Ansprüchen 11 oder 12, ferner umfassend die folgenden Schritte:Schritt c), wobei das selektive Erhitzen das Lesen der maschinenlesbaren Daten umfaßt, um die Auftragefläche zu definieren.e) Definieren der Umfangskanten (20) des graphischen Produkts (13) als maschinenlesbare Daten;f) Speichern der maschinenlesbaren Daten, welche die Umfangskanten des graphischen Produkts (13) definieren;g) Selektieren des einen Bereichs (13 oder 46, 48) der Bereiche der Blattmaterialschicht zum Trennen von der Trägerschicht (17); und
- Verfahren zum Herstellen eines graphischen Produkts nach den Ansprüchen 11, 12 oder 13, wobei Schritt c) des selektiven Erhitzens umfaßt:c2) zur Verfügung Stellen des Hitzemittels (101); undc3) Transportieren der lösbar an einer Trägerschicht (17) befestigten Blattmaterialschicht (16) und der darüberliegenden haftenden Bahn (15) relativ zu dem Hitzemittel.
- Verfahren zum Herstellen eines graphischen Produkts nach Anspruch 14, wobei das Hitzemittel einen Thermokopf (101) mit mehreren einzeln aktivierbaren Hitzeelementen umfaßt.
- Verfahren zum Herstellen eines graphischen Produkts nach Anspruch 15, das folgende zusätzliche Schritte umfaßt:h) Definieren der Umfangskanten (20) des graphischen Produkts als maschinenlesbare Daten und Speichern der maschinenlesbaren Daten zum darauffolgenden Abrufen; undi) den Schritt des selektiven Erhitzens, wobei dieser das Anregen der Hitzeelemente entsprechend der maschinenlesbaren Daten umfaßt, um die haftende Bahn (15) über die Auftragefläche zu erhitzen.
- Verfahren nach Anspruch 16, ferner umfassend die Schritte des Pressens des Thermokopfs (101) gegen die haftende Bahn (15) und die Blattmaterialschicht (16) auf der Trägerschicht (17) während des Schritts des selektiven Erhitzens, um die haftende Bahn mit dem einen (13 oder 46, 48) der Bereiche zu verbinden.
- Verfahren zum Herstellen eines graphischen Produkts nach einem der Ansprüche 11 bis 17, wobei der darunterliegende Bereich der Bereiche den Ausschuß bildet (46, 48).
- Verfahren zum Herstellen eines graphischen Produkts nach Anspruch 18, ferner umfassend die folgenden Schritte:k) Wiederholen der Schritte a) und c) des Plazierens und selektiven Erhitzens, wobei der darunterliegende Bereich der Bereiche das graphische Produkt (13) ist; und anschließendl) das Abtrennen der haftenden Bahn (15) und des haftenden graphischen Produkts (13) von der Trägerschicht (17);m) Übergabe des graphischen Produkts an ein Zeichensubstrat, während das graphische Produkt an der haftenden Bahn haftet; und sodannn) Abnehmen der haftenden Bahn von dem graphischen Produkt auf dem Zeichensubstrat.
- Verfahren zum Herstellen eines graphischen Produkts nach den Ansprüchen 18 oder 19, wobei die Blattmaterialschicht (16) ein Vinylblattmaterial umfaßt und die Trägerschicht (17) auf einer Seite ein Lösematerial hat, und wobei das Vinylblattmaterial durch ein druckempfindliches Klebemittel (38), das eine temporäre Haftung bildet, lösbar an dem Lösematerial der Trägerschicht befestigt ist, und das hitzeaktivierbare Klebemittel zwischen der haftenden Bahn und dem Ausschuß eine Haftung erzeugt, die stärker ist als die temporäre Haftung.
- Verfahren zum Herstellen eines graphischen Produkts nach Anspruch 20, wobei
Schritt c) des selektiven Erhitzens ferner das Erhitzen der Trägerschicht (17) und das Lösen des druckempfindlichen Klebemittels (38) entlang der Umfangskanten vor dem Schritt des Abtrennens umfaßt, um das Entfernen des Ausschusses (46, 48) zu erleichtern. - Verfahren zum Herstellen eines graphischen Produkts (13), umfassend die folgenden Schritte:a) zur Verfügung Stellen eines Blattmaterials (16), das mittels eines drukkempfindlichen Klebemittels lösbar an einer Trägerschicht (17) befestigt ist, wobei ein Bereich (13) der Blattmaterialschicht ein graphisches Produkt definiert, das entlang Schnittlinien an den Umfangskanten (20) des graphischen Produkts von dem übrigen Bereich (46, 48) der Blattmaterialschicht abgetrennt wird;b) Plazieren einer Anti-Haft-Bahn mit einem Hemmstoff für hitzeaktivierte Klebemittel derart, daß sie die Blattmaterialschicht (16) überdeckt, wobei der Hemmstoff für hitzeaktivierte Klebemittel zwischen der Blattmaterialschicht und der Anti-Haft-Bahn angeordnet ist;c) Selektives Erhitzen der Anti-Haft-Bahn mittels selektiv anregbarer Hitzeemente über eine Auftragefläche, die dem im wesentlichen gesamten übrigen Bereich der Blattmaterialschicht entspricht, um den Haft-Hemmstoff auf den im wesentlichen gesamten übrigen Bereich aufzutragen;d) Plazieren einer Übergabebahn mit einer Haftbeschichtung, derart, daß sie die Blattmaterialschicht überdeckt, um die Übergabebahn mit dem Bereich (13) der Blattmaterialschicht, der das graphische Produkt definiert und auf dem kein Haft-Hemmstoff aufgetragen ist, zu verbinden;e) Abtrennen der Übergabebahn zusammen mit dem Bereich (13), der das graphische Produkt definiert, von der Trägerschicht; undf) Plazieren der Übergabebahn und des Bereichs, der das graphische Produkt definiert, derart auf einem Graphikprodukt-Substrat, daß ermöglicht wird, daß das druckempfindliche Klebemittel das graphische Produkt an das Substrat bindet.
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP00104347A EP1129867B1 (de) | 2000-03-02 | 2000-03-02 | Verfahren und Vorrichtung zur Herstellung eines graphischen Produkts |
| AT00104347T ATE229886T1 (de) | 2000-03-02 | 2000-03-02 | Verfahren und vorrichtung zur herstellung eines graphischen produkts |
| DE60001045T DE60001045T2 (de) | 2000-03-02 | 2000-03-02 | Verfahren und Vorrichtung zur Herstellung eines graphischen Produkts |
| ES00104347T ES2188439T3 (es) | 2000-03-02 | 2000-03-02 | Procedimiento y dispositivo para fabricar productos graficos. |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP00104347A EP1129867B1 (de) | 2000-03-02 | 2000-03-02 | Verfahren und Vorrichtung zur Herstellung eines graphischen Produkts |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1129867A1 EP1129867A1 (de) | 2001-09-05 |
| EP1129867B1 true EP1129867B1 (de) | 2002-12-18 |
Family
ID=8168009
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP00104347A Expired - Lifetime EP1129867B1 (de) | 2000-03-02 | 2000-03-02 | Verfahren und Vorrichtung zur Herstellung eines graphischen Produkts |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP1129867B1 (de) |
| AT (1) | ATE229886T1 (de) |
| DE (1) | DE60001045T2 (de) |
| ES (1) | ES2188439T3 (de) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| NL2015230B1 (nl) * | 2015-07-28 | 2017-02-20 | W R R Holding Leiden B V | Meerlaags foliesamenstel en werkwijze ter vorming van een markering. |
| FI130466B (en) * | 2021-05-04 | 2023-09-19 | Teknologian Tutkimuskeskus Vtt Oy | IMPROVED ROLL-TO-ROLL PROCESS METHOD |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5026584A (en) * | 1987-05-29 | 1991-06-25 | Gerber Scientific Products, Inc. | Sign making web with dry adhesive layer |
| US5143576A (en) * | 1990-08-10 | 1992-09-01 | Gerber Scientific Products, Inc. | Automatic weeding system and method of use |
| US5537135A (en) * | 1993-01-22 | 1996-07-16 | Gerber Scientific Products, Inc. | Method and apparatus for making a graphic product |
| US5645932A (en) * | 1993-12-30 | 1997-07-08 | Kabushiki Kaisha Miyake | Circuit-like metallic foil sheet and the like and process for producing them |
| JP3116209B2 (ja) * | 1994-12-01 | 2000-12-11 | 株式会社三宅 | 共振タグ等の回路様金属箔シートの製造方法 |
| US5727887A (en) * | 1996-04-08 | 1998-03-17 | Gerber Scientific Products, Inc. | Apparatus and method for performing a work operation with a consumable web |
-
2000
- 2000-03-02 AT AT00104347T patent/ATE229886T1/de not_active IP Right Cessation
- 2000-03-02 ES ES00104347T patent/ES2188439T3/es not_active Expired - Lifetime
- 2000-03-02 EP EP00104347A patent/EP1129867B1/de not_active Expired - Lifetime
- 2000-03-02 DE DE60001045T patent/DE60001045T2/de not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| ATE229886T1 (de) | 2003-01-15 |
| DE60001045D1 (de) | 2003-01-30 |
| ES2188439T3 (es) | 2003-07-01 |
| DE60001045T2 (de) | 2003-09-04 |
| EP1129867A1 (de) | 2001-09-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US6102097A (en) | Apparatus for manufacturing a graphic product | |
| US6085818A (en) | Printed label, method and apparatus for manufacturing printed labels, and method and apparatus for attaching printed labels | |
| AU673526B2 (en) | Linerless label printer applicator | |
| US5466501A (en) | Sign making web with tack killing overcoat removable by washing and related method | |
| EP0470645B1 (de) | System zum Trennen von geschnittenen Produkten und Methode zur Anwendung | |
| AU753397B2 (en) | Apparatus and method for applying linerless labels | |
| US5651846A (en) | Method and apparatus for removing the printed layer of labels from semirigid containers | |
| EP1390201B1 (de) | Automatisches verfahren und automatische vorrichtung zur entfernung von abfallbereichen | |
| EP0199810A1 (de) | Verbesserungen an und betreffend die herstellung von transferts. | |
| EP1129867A1 (de) | Verfahren und Vorrichtung zur Herstellung eines graphischen Produkts | |
| US7124524B2 (en) | Tag with folding reinforcement | |
| JP3442339B2 (ja) | グラフィック製品作製方法および装置 | |
| EP0119669A1 (de) | Verfahren zum Etikettieren von Gegenständen | |
| JP3366745B2 (ja) | ラベル貼付方法 | |
| JP2001030385A (ja) | タックラベルの製造方法及び製造装置 | |
| JP3813198B2 (ja) | 印字ラベルの製造装置及びその製造方法 | |
| JP2550736Y2 (ja) | 感熱ラベラー | |
| JP3224633U (ja) | シート貼付装置 | |
| JP3734185B2 (ja) | ラベル連続体の製造方法 | |
| US6729374B2 (en) | Label laminating device | |
| JP2513265Y2 (ja) | 瓶容器への首掛け用ラベルの装置用帯状材 | |
| JP2923143B2 (ja) | 意匠刻設方法 | |
| US20250206054A1 (en) | Thermal printable medium, method for producing the thermal printable medium, use of the thermal printable medium and system comprising thermal printing device and thermal printable medium | |
| US6401782B1 (en) | Label laminating device | |
| AU720751B2 (en) | Improved manufacturing method and apparatus for adhesive labels |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20000302 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| 17Q | First examination report despatched |
Effective date: 20011106 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| AKX | Designation fees paid |
Free format text: AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20021218 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20021218 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20021218 |
|
| REF | Corresponds to: |
Ref document number: 229886 Country of ref document: AT Date of ref document: 20030115 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 60001045 Country of ref document: DE Date of ref document: 20030130 Kind code of ref document: P |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030302 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030302 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030303 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030318 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20030318 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20030331 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: SCHMAUDER & PARTNER AG PATENTANWALTSBUERO |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2188439 Country of ref document: ES Kind code of ref document: T3 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20030919 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20040302 Year of fee payment: 5 Ref country code: SE Payment date: 20040302 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20040303 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050302 Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050302 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050303 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050331 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050331 |
|
| EUG | Se: european patent has lapsed | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: 732E |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20090923 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20090924 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20090930 Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20091008 Year of fee payment: 10 |
|
| BERE | Be: lapsed |
Owner name: *GERBER SCIENTIFIC PRODUCTS INC. Effective date: 20100331 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20100302 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20101130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100331 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20101001 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100302 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20110415 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110404 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100303 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20091006 Year of fee payment: 10 |